WO2024057560A1 - 粘着シート - Google Patents
粘着シート Download PDFInfo
- Publication number
- WO2024057560A1 WO2024057560A1 PCT/JP2022/045742 JP2022045742W WO2024057560A1 WO 2024057560 A1 WO2024057560 A1 WO 2024057560A1 JP 2022045742 W JP2022045742 W JP 2022045742W WO 2024057560 A1 WO2024057560 A1 WO 2024057560A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- weight
- less
- adhesive layer
- adhesive sheet
- adhesive
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J133/00—Adhesives based on homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by only one carboxyl radical, or of salts, anhydrides, esters, amides, imides, or nitriles thereof; Adhesives based on derivatives of such polymers
- C09J133/04—Homopolymers or copolymers of esters
- C09J133/06—Homopolymers or copolymers of esters of esters containing only carbon, hydrogen and oxygen, the oxygen atom being present only as part of the carboxyl radical
- C09J133/08—Homopolymers or copolymers of acrylic acid esters
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L33/00—Compositions of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and only one being terminated by only one carboxyl radical, or of salts, anhydrides, esters, amides, imides or nitriles thereof; Compositions of derivatives of such polymers
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J11/00—Features of adhesives not provided for in group C09J9/00, e.g. additives
- C09J11/02—Non-macromolecular additives
- C09J11/04—Non-macromolecular additives inorganic
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J11/00—Features of adhesives not provided for in group C09J9/00, e.g. additives
- C09J11/02—Non-macromolecular additives
- C09J11/06—Non-macromolecular additives organic
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J11/00—Features of adhesives not provided for in group C09J9/00, e.g. additives
- C09J11/08—Macromolecular additives
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J133/00—Adhesives based on homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by only one carboxyl radical, or of salts, anhydrides, esters, amides, imides, or nitriles thereof; Adhesives based on derivatives of such polymers
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J133/00—Adhesives based on homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by only one carboxyl radical, or of salts, anhydrides, esters, amides, imides, or nitriles thereof; Adhesives based on derivatives of such polymers
- C09J133/04—Homopolymers or copolymers of esters
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J7/00—Adhesives in the form of films or foils
- C09J7/10—Adhesives in the form of films or foils without carriers
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J7/00—Adhesives in the form of films or foils
- C09J7/30—Adhesives in the form of films or foils characterised by the adhesive composition
- C09J7/38—Pressure-sensitive adhesives [PSA]
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J7/00—Adhesives in the form of films or foils
- C09J7/30—Adhesives in the form of films or foils characterised by the adhesive composition
- C09J7/38—Pressure-sensitive adhesives [PSA]
- C09J7/381—Pressure-sensitive adhesives [PSA] based on macromolecular compounds obtained by reactions involving only carbon-to-carbon unsaturated bonds
- C09J7/385—Acrylic polymers
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J2301/00—Additional features of adhesives in the form of films or foils
- C09J2301/30—Additional features of adhesives in the form of films or foils characterized by the chemical, physicochemical or physical properties of the adhesive or the carrier
- C09J2301/312—Additional features of adhesives in the form of films or foils characterized by the chemical, physicochemical or physical properties of the adhesive or the carrier parameters being the characterizing feature
Definitions
- the present invention relates to an adhesive sheet.
- This application claims priority based on Japanese Patent Application No. 2022-145689 filed on September 13, 2022, and the entire contents of that application are incorporated herein by reference.
- adhesives also referred to as pressure-sensitive adhesives, hereinafter the same
- adhesives exhibit a soft solid (viscoelastic) state in the temperature range around room temperature, and have the property of easily adhering to adherends under pressure.
- adhesives are used in various industrial fields, from mobile electronic devices such as smartphones and home appliances to automobiles and office automation equipment, to attach parts to parts, typically in the form of adhesive sheets containing an adhesive layer. It is widely used for purposes such as bonding and surface protection. Preferred examples of uses of such adhesive sheets include joining, fixing, and protecting members within electronic devices.
- Patent Document 1 can be cited as a document related to this type of technology.
- Patent Documents 2 and 3 are prior art documents that disclose adhesives containing acrylic polymers polymerized using heptyl acrylate as a monomer component.
- Adhesive sheets used for the purpose of concealing adherends, adjusting their appearance, adding design, etc. accomplish their purposes by covering the entire visible surface of the adherend. Since such pressure-sensitive adhesive sheets can be visually recognized from the outside, they are required to have good appearance quality. For example, in the display section of electronic devices, adhesive sheets used to hide metal components placed on the back side of organic EL panels, etc., can come into contact with the user's eyes when the display section is turned off, so the appearance It is required to cover the adherend with good quality.
- adhesive sheets are usually made of adhesive sheets with a release liner whose adhesive surface is protected by a release liner from the viewpoint of productivity and handling. handled in form.
- the adhesive surface is kept smooth and adheres well to the surface of the adherend to exhibit the desired adhesive properties.
- the adhesive sheet having the adhesive surface protected by a release liner and held smooth can be uniformly applied to an adherend and provide a good appearance when the adherend surface is visually recognized. .
- Such a pressure-sensitive adhesive sheet with a release liner is, for example, formed into a roll body (adhesive sheet roll with a release liner) in which the pressure-sensitive adhesive sheet with a release liner is wound, and distributed, stored, and subjected to processing.
- a pressure-sensitive adhesive sheet whose adhesive layer is colored, such as containing a coloring agent tends to exhibit more contrast in uneven deformation than a transparent pressure-sensitive adhesive sheet, and changes in appearance due to the uneven deformation tend to be more noticeable.
- the present invention was created in view of the above circumstances, and an object of the present invention is to provide a pressure-sensitive adhesive sheet that can highly suppress fine uneven deformation.
- a pressure-sensitive adhesive sheet having a colored pressure-sensitive adhesive layer contains an acrylic polymer. Moreover, the gel fraction of the adhesive layer is 25% or more. Furthermore, the adhesive layer has a storage modulus of 0.05 MPa or more at 23°C, and a tan ⁇ of 0.31 or more at 23°C.
- tan ⁇ refers to the ratio (G''/G') of the loss elastic modulus G'' to the storage elastic modulus G' of the adhesive layer.
- the adhesive layer containing the acrylic polymer has a gel fraction of 25% or more, a storage modulus of 0.05 MPa or more at 23°C, and has appropriate hardness. Irregular deformation is less likely to occur.
- the adhesive layer has a tan ⁇ of 0.31 or more at 23° C., so it has good relaxation properties. Therefore, when fine uneven deformation occurs in the adhesive layer, such as dents on the adhesive surface, the fine uneven deformation is canceled or softened by the relaxing action of the adhesive. Since the above-mentioned pressure-sensitive adhesive sheet has a colored adhesive layer, uneven deformation tends to be noticeable. However, with a configuration including an adhesive layer that satisfies the above characteristics, fine uneven deformation is highly suppressed, so it is an excellent product. It has good appearance quality.
- the monomer component constituting the acrylic polymer includes an alkyl acrylate having a chain alkyl group having 4 to 8 carbon atoms.
- an acrylic polymer containing as a monomer component an alkyl acrylate having a chain alkyl group having 4 to 8 carbon atoms (C 4-8 alkyl acrylate)
- adhesiveness that achieves both the above-mentioned storage modulus at 23°C and tan ⁇ at 23°C is achieved. It is easy to form a drug layer.
- the technology disclosed herein is preferably implemented in an embodiment using an acrylic polymer containing C 4-8 alkyl acrylate as a monomer component.
- the monomer component constituting the acrylic polymer includes heptyl acrylate.
- heptyl acrylate By using an acrylic polymer containing heptyl acrylate as a monomer component, it is easy to form an adhesive having a storage modulus at 23° C. of a predetermined value or more and a high tan ⁇ at 23° C.
- the monomer component constituting the acrylic polymer includes n-butyl acrylate. According to the technology disclosed herein, it is possible to obtain an adhesive that has both the above-mentioned storage modulus at 23°C and tan ⁇ at 23°C with a composition using an acrylic polymer containing n-butyl acrylate as a monomer component.
- the adhesive layer includes a black colorant.
- a black colorant When using a small amount of black colorant, light transmittance can be efficiently adjusted, and high covering properties can easily be obtained.
- the effect of the technology disclosed herein high degree of suppression of fine unevenness deformation) can be effectively exhibited in a pressure-sensitive adhesive sheet having a pressure-sensitive adhesive layer containing a black colorant.
- the adhesive layer includes a black colorant as a first colorant and a metal oxide as a second colorant.
- the adhesive layer further includes a tackifier resin.
- a tackifying resin By including a tackifying resin, adhesive strength can be improved. According to the technology disclosed herein, it is possible to form an adhesive layer with a composition containing a tackifying resin that satisfies the above gel fraction, 23°C storage modulus, and 23°C tan ⁇ , and achieve the desired effect. .
- the adhesive layer further includes an acrylic oligomer.
- Adhesive strength can be improved by including an acrylic oligomer.
- the pressure-sensitive adhesive sheet is a base material-less double-sided pressure-sensitive adhesive sheet comprising the pressure-sensitive adhesive layer. Since the base material-less double-sided pressure-sensitive adhesive sheet does not have a base material, it can be made thinner, and can contribute to miniaturization and space saving of products to which the double-sided pressure-sensitive adhesive sheet is applied. Moreover, according to the base material-less double-sided pressure-sensitive adhesive sheet, the effects of the pressure-sensitive adhesive layer, such as adhesive strength, can be maximized. Further, the effects of the technology disclosed herein can be effectively exhibited in a base material-less double-sided pressure-sensitive adhesive sheet.
- the adhesive sheet disclosed herein can be preferably used, for example, to bond members of electronic devices including home appliances, office automation equipment, and portable electronic devices such as smartphones.
- electronic devices have parts that are visible to users, and may be required to have excellent appearance quality.
- the pressure-sensitive adhesive sheet disclosed herein has highly suppressed deformation of fine irregularities and has excellent appearance quality, so it can be applied to visible parts of electronic devices to realize a surface with good appearance quality.
- this specification provides an electronic device using any of the adhesive sheets disclosed herein, in other words, an electronic device including the adhesive sheet.
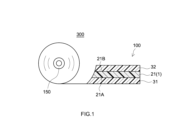
- FIG. 1 is a cross-sectional view schematically showing the configuration of a pressure-sensitive adhesive sheet according to an embodiment.
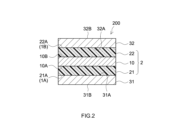
- FIG. 3 is a cross-sectional view schematically showing the configuration of a pressure-sensitive adhesive sheet according to another embodiment.
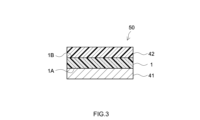
- FIG. 2 is a cross-sectional view schematically showing an example of the structure of a laminate.
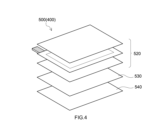
- FIG. 1 is an exploded perspective view schematically showing a configuration example of a display device.
- the term "adhesive” as used herein refers to a material that exhibits a soft solid (viscoelastic) state in the temperature range around room temperature and has the property of easily adhering to an adherend under pressure. .
- the adhesive referred to here generally has a complex tensile modulus E * (1Hz) as defined in "C. A. Dahlquist, “Adhesion: Fundamentals and Practice", McLaren & Sons, (1966) P. 143". ⁇ 10 7 dyne/cm 2 (typically, a material having the above properties at 25° C.).
- biomass-derived carbon means carbon derived from biomass materials, that is, materials derived from renewable organic resources (renewable carbon).
- biomass materials are typically materials derived from biological resources (typically plants that perform photosynthesis) that can be reproduced sustainably in the presence of sunlight, water, and carbon dioxide. means. Therefore, materials derived from fossil resources that are depleted through use after mining (fossil resource-based materials) are excluded from the concept of biomass materials here.
- the biomass carbon ratio of the adhesive layer and the adhesive sheet that is, the proportion of biomass-derived carbon in the total carbon contained in the adhesive layer and the adhesive sheet, is the carbon isotope content with a mass number of 14 measured in accordance with ASTM D6866. It can be estimated from the amount.
- the adhesive sheet disclosed herein includes an adhesive layer.
- the above-mentioned pressure-sensitive adhesive sheet is, for example, a base material-less double-sided pressure-sensitive adhesive sheet comprising a first pressure-sensitive adhesive surface formed by one surface of the pressure-sensitive adhesive layer, and a second pressure-sensitive adhesive surface formed by the other surface of the pressure-sensitive adhesive layer.
- the pressure-sensitive adhesive sheet disclosed herein may be in the form of a pressure-sensitive adhesive sheet with a base material, in which the pressure-sensitive adhesive layer is laminated on one or both sides of a support base material.
- the supporting base material may be simply referred to as "base material”.
- adhesive sheet here may include what is called an adhesive tape, an adhesive label, an adhesive film, and the like.
- the pressure-sensitive adhesive sheet disclosed herein may be in the form of a roll or a sheet. Alternatively, the adhesive sheet may be further processed into various shapes.
- FIG. 1 The structure of a pressure-sensitive adhesive sheet according to one embodiment is schematically shown in FIG.
- This adhesive sheet 1 is configured as a double-sided adhesive sheet without a base material, which includes an adhesive layer 21.
- the adhesive layer 21 is colored.
- the adhesive sheet 1 has a first adhesive surface 21A constituted by one surface (first surface) of the adhesive layer 21 and a second adhesive surface constituted by the other surface (second surface) of the adhesive layer 21. 21B are attached to different parts of the adherend.
- the locations on which the adhesive surfaces 21A and 21B are attached may be on different members, or may be on different locations within a single member. As shown in FIG.
- the adhesive sheet 1 before use (that is, before being attached to an adherend) has a first adhesive surface 21A and a second adhesive surface 21B that are peeled off at least on the side facing the adhesive layer 21. It may be a component of the adhesive sheet 100 with a release liner that is protected by the release liners 31 and 32 serving as surfaces.
- the release liners 31 and 32 it is preferable to use, for example, a sheet-like base material (liner base material) that has a release layer formed of a release treatment agent on one side so that one side becomes a release surface. obtain.
- the release liner 32 may be omitted and a release liner 31 having release surfaces on both sides may be used, and this and the adhesive sheet 1 may be overlapped and spirally wound so that the second adhesive surface 21B is on the release liner 31.
- the pressure-sensitive adhesive sheet with a release liner may be in a protected form (roll form) in contact with the back surface of the adhesive sheet.
- the adhesive sheet 100 with a release liner may be in the form of a roll body (adhesive sheet roll with a release liner) 300 as shown in FIG.
- a roll body adheresive sheet roll with a release liner
- Such an adhesive sheet roll 300 has a release liner-equipped adhesive sheet 100 wound around a core 150.
- FIG. 2 The structure of a pressure-sensitive adhesive sheet according to another embodiment is schematically shown in FIG. 2.
- This adhesive sheet 2 includes a sheet-shaped support base material (for example, a resin film) 10 having a first surface 10A and a second surface 10B, and a first adhesive layer 21 fixedly provided on the first surface 10A side. and a second adhesive layer 22 fixedly provided on the second surface 10B side.
- both the first adhesive layer 21 and the second adhesive layer 22 are colored.
- 32 may be a component of the adhesive sheet 200 with a release liner.
- the release liner 32 may be omitted and a release liner 31 having release surfaces on both sides may be used, and this and the adhesive sheet 2 may be overlapped and spirally wound so that the second adhesive surface 22A is on the release liner 31.
- the pressure-sensitive adhesive sheet with a release liner may be in a protected form (roll form) in contact with the back surface of the adhesive sheet.
- Such a double-sided pressure-sensitive adhesive sheet with a base material is preferable because it has excellent processability, handling properties, and the like.
- both the first adhesive layer and the second adhesive layer may not be colored, and at least one of the first adhesive layer and the second adhesive layer may be configured as a colored adhesive layer. All you have to do is stay there.
- the technology disclosed herein can be preferably implemented in the form of a base material-less double-sided adhesive sheet. Since the base material-less double-sided pressure-sensitive adhesive sheet does not have a supporting base material, it is easy to form a thin layer, and is also advantageous in that it can maximize adhesive properties such as adhesive strength and impact resistance. In addition, the base material-less double-sided adhesive sheet can make full use of the thickness of the adhesive layer to alleviate minute irregularities that occur in the adhesive layer.
- an adhesive layer in an embodiment including a first adhesive layer and a second adhesive layer, at least one of the first adhesive layer and the second adhesive layer; particularly The same applies hereinafter unless otherwise specified
- a pressure-sensitive adhesive sheet having a colored pressure-sensitive adhesive layer can hide an adherend. Furthermore, by adjusting the degree of coloring of the adhesive layer, it is possible to adjust optical properties such as light transmittance, and to impart design and color to the surface of the adherend.
- the adhesive layer disclosed herein has a storage modulus at 23°C (23°C storage modulus) of 0.05 MPa or more. Since the adhesive layer that satisfies the above 23° C. storage modulus has appropriate hardness, it is difficult for visible uneven deformation to occur. In some preferred embodiments, the 23°C storage modulus is approximately 0.06 MPa or more, may be 0.07 MPa or more, or may be 0.08 MPa or more. Since the pressure-sensitive adhesive layer having the above-mentioned 23° C. storage modulus has an appropriate cohesive force, it tends to provide high adhesion reliability to the adherend. In addition, they tend to have excellent workability. Further, in some embodiments, the 23° C.
- storage modulus of the adhesive layer is approximately 0.60 MPa or less, may be approximately 0.40 MPa or less, or may be approximately 0.20 MPa or less.
- An adhesive layer having a storage modulus at 23° C. of a predetermined value or less tends to have adhesive properties to an adherend. In some preferred embodiments, it is approximately 0.18 MPa or less, more preferably 0.15 MPa or less, even more preferably 0.13 MPa or less, may be 0.11 MPa or less, and may be less than 0.10 MPa, It may be 0.08 MPa or less.
- the adhesive layer disclosed herein is characterized by the above-mentioned 23°C storage modulus of 0.05 MPa or more and tan ⁇ at 23°C (23°C tan ⁇ ) of 0.31 or more. Can be attached.
- the above tan ⁇ (loss tangent) refers to the ratio (G''/G') of the loss elastic modulus G'' to the storage elastic modulus G' of the adhesive layer.
- An adhesive layer with a tan ⁇ of 0.31 or more at 23°C has good relaxation properties, so minute deformations in the adhesive layer, such as dents on the adhesive surface, can be easily resolved in a short time due to the relaxation effect of the adhesive. Alleviated, resolved or softened.
- the 23°C tan ⁇ may be 0.40 or more, 0.45 or more, 0.50 or more, or 0.55 or more. In some preferred embodiments, the 23°C tan ⁇ is 0.60 or more, more preferably 0.65 or more, and still more preferably 0.70 or more.
- the above 23°C tan ⁇ usually tends to decrease as the 23°C storage modulus increases, so it is preferable that the upper limit of the 23°C tan ⁇ be within an appropriate range that is compatible with the 23°C storage modulus. . In some embodiments, the 23°C tan ⁇ is 3 or less, may be 1.5 or less, may be 1.2 or less, or may be 1.0 or less.
- the 23°C tan ⁇ is less than 1.0, may be less than 0.95, may be less than 0.90, and may be less than 0.85. It may be less than 0.80, or less than 0.75. In some other embodiments, the 23°C tan ⁇ may be 0.70 or less, 0.65 or less, 0.60 or less, or 0.55 or less.
- the 23°C storage elastic modulus and 23°C tan ⁇ of the adhesive layer can be determined by dynamic viscoelasticity measurement.
- a pressure-sensitive adhesive layer with a thickness of about 2 mm is produced by stacking a plurality of pressure-sensitive adhesive layers to be measured (in the case of a double-sided pressure-sensitive adhesive sheet without a base material, double-sided pressure-sensitive adhesive sheets). A sample of this adhesive layer was punched into a disk shape with a diameter of 7.9 mm, which was sandwiched and fixed between parallel plates. Dynamic viscoelasticity measurement is performed under the following conditions to determine the 23°C storage modulus and the 23°C tan ⁇ .
- ⁇ Measurement mode Shear mode ⁇ Temperature range: -70°C ⁇ 150°C ⁇ Heating rate: 5°C/min ⁇ Measurement frequency: 1Hz
- the above-mentioned method is also used in the Examples described below.
- the adhesive layer to be measured may be formed by applying a corresponding adhesive composition in a layered manner and drying or curing it.
- the light transmittance of a colored adhesive layer varies depending on the purpose of use and the purpose of coloring, and is not limited to a specific range, but usually, a colored adhesive layer has a higher light transmittance than a transparent adhesive layer. It also has low light transmittance.
- the light transmittance at a wavelength of 550 nm (550 nm light transmittance, also referred to as visible light transmittance) of the adhesive layer is less than 80%, may be less than 70%, and may be less than 60%. It may be less than 50%, or less than 40%.
- a pressure-sensitive adhesive sheet whose visible light transmittance is reduced by coloring the pressure-sensitive adhesive layer is suitable for hiding an adherend, and can also be used to impart design properties. It can also be used as a light-shielding adhesive sheet for purposes such as preventing light leakage.
- the 550 nm light transmittance of the adhesive layer is 30% or less, may be 20% or less, may be 15% or less, may be 10% or less, may be 8% or less, It may be 6% or less. The lower the visible light transmittance, the more excellent hiding power can be exhibited. When higher hiding power is required, the 550 nm light transmittance may be less than 5%, less than 4%, less than 3%, less than 2%, less than 1%, or 0.
- the lower limit of the 550 nm light transmittance is not particularly limited, and may be substantially 0%, that is, below the detection limit, 0.1% or more, 1% or more, or 3% or more. Often, it may be 5% or more. In some embodiments, the 550 nm light transmittance may be 10% or more, more than 20%, or more than 30%.
- an adhesive layer having appropriate light transmittance is preferable from the viewpoint of maintaining adhesive properties and productivity.
- the light transmittance of the adhesive layer at a wavelength of 1380 nm (1380 nm light transmittance, also referred to as infrared transmittance) is less than 90%, may be less than 80%, and may be less than 70%. It may be less than 60%, less than 50%, or less than 40%.
- the 1380 nm light transmittance of the adhesive layer is 30% or less, may be 20% or less, may be 15% or less, may be 10% or less, may be 5% or less, It may be 3% or less.
- the pressure-sensitive adhesive layer with limited infrared transmittance can block light in a wide wavelength range including infrared rays, making it easy to obtain excellent light blocking properties.
- the lower limit of the 1380 nm light transmittance is not particularly limited, and may be substantially 0%, that is, below the detection limit, 0.1% or more, 1% or more, or 3% or more. Often, it may be 5% or more. In some embodiments, the 1380 nm light transmittance may be 10% or more, 30% or more, or 50% or more.
- the relative relationship between the visible light transmittance and the infrared transmittance of the adhesive layer is not particularly limited.
- the ratio (T IR /T VL ) of the infrared transmittance T IR [%] and the visible light transmittance T VL [%] of the adhesive layer is, for example, within a range of 0.1 to 10. It may be 5 or less, 3 or less, 0.5 or more, 1 or more (for example, more than 1), or 2 or more.
- the light transmittance [%] of the pressure-sensitive adhesive layer and pressure-sensitive adhesive sheet is determined by using a commercially available spectrophotometer. It is determined by measuring the light transmittance (light transmittance at 550 nm and 1380 nm).
- a spectrophotometer manufactured by Hitachi device name: "U4150 type spectrophotometer" or its equivalent is used. Note that the light transmittances at wavelengths of 550 nm and 1380 nm correspond to visible light transmittance and infrared transmittance, respectively.
- the above-mentioned light transmittance of the base material-less double-sided pressure-sensitive adhesive sheet consisting of the pressure-sensitive adhesive layer is also the light transmittance of the pressure-sensitive adhesive layer.
- the adhesive layer constituting the adhesive sheet disclosed herein contains an acrylic polymer.
- the pressure-sensitive adhesive layer is typically a pressure-sensitive adhesive layer containing an acrylic polymer as a base polymer.
- Such an adhesive layer is also referred to as an acrylic adhesive layer.
- the base polymer refers to the main component of a rubbery polymer (a polymer that exhibits rubber elasticity in a temperature range around room temperature) contained in the adhesive layer.
- the term "main component” refers to a component contained in an amount exceeding 50% by weight, unless otherwise specified.
- the following description regarding the adhesive and the components that can be included in the adhesive layer is also applicable to the adhesive composition used to form the adhesive (layer) unless otherwise specified.
- the term "acrylic polymer” refers to a polymer containing monomer units derived from a monomer having at least one (meth)acryloyl group in one molecule, as monomer units constituting the polymer. .
- a monomer having at least one (meth)acryloyl group in one molecule will also be referred to as an "acrylic monomer.”
- an acrylic polymer in this specification is defined as a polymer containing monomer units derived from acrylic monomers.
- (meth)acryloyl” refers comprehensively to acryloyl and methacryloyl.
- (meth)acrylate” comprehensively refers to acrylate and methacrylate
- (meth)acrylic” comprehensively refers to acrylic and methacrylic.
- the acrylic polymer in the technology disclosed herein for example, a polymer of a monomer raw material containing an alkyl (meth)acrylate as a main monomer and which may further contain a submonomer copolymerizable with the main monomer is preferable.
- the main monomer refers to a component that accounts for more than 50% by weight of the monomer composition in the monomer raw material.
- alkyl (meth)acrylate for example, a compound represented by the following formula (1) can be suitably used.
- CH 2 C(R 1 )COOR 2 (1)
- R 1 in the above formula (1) is a hydrogen atom or a methyl group.
- R 2 is a chain alkyl group having 1 to 20 carbon atoms.
- such a range of the number of carbon atoms may be expressed as "C 1-20 ".
- an alkyl (meth)acrylate in which R 2 is a C 1-14 (for example, C 1-10 , typically C 4-8 ) chain alkyl group is used as the main monomer. It is appropriate to do so.
- alkyl (meth)acrylates in which R 2 is a C 1-20 chain alkyl group include, but are not limited to, methyl (meth)acrylate, ethyl (meth)acrylate, propyl (meth)acrylate, and isopropyl.
- the proportion of alkyl (meth)acrylate in the monomer components constituting the acrylic polymer is typically more than 50% by weight, for example, it can be 70% by weight or more, it may be 85% by weight or more, and it can be 90% by weight or more. It may be more than 90% by weight (for example, more than 90% by weight), suitably more than 92% by weight, more than 94% by weight, and more than 95% by weight.
- the upper limit of the proportion of alkyl (meth)acrylate is not particularly limited, but it is preferably 99.5% by weight or less (for example, 99% by weight or less), or characteristics based on submonomers such as carboxy group-containing monomers (for example, aggregation). From the viewpoint of preferably exerting the force), the content may be 98% by weight or less (for example, less than 97% by weight).
- the acrylic polymer may be obtained by polymerizing substantially only alkyl (meth)acrylate.
- an alkyl acrylate in which R 1 in the above formula (1) is a hydrogen atom and R 2 is a C 4-8 chain alkyl group (hereinafter also simply referred to as a C 4-8 alkyl acrylate). ) is preferably used as the main monomer.
- an acrylic polymer containing C 4-8 alkyl acrylate as a monomer component it is easy to form an adhesive layer that achieves both the above-mentioned 23°C storage modulus and 23°C tan ⁇ .
- the proportion of C 4-8 alkyl acrylate contained in the monomer component is, for example, more than 50% by weight, preferably 70% by weight or more, and 90% by weight or more. It is more preferably 92% by weight or more, more preferably 92% by weight or more, and may be 94% by weight or more (for example, more than 95% by weight).
- the upper limit of the proportion of C 4-8 alkyl acrylate is not particularly limited, but it is preferably 99% by weight or less, for example, from the viewpoint of preferably exhibiting the characteristics (for example, cohesive force) based on the submonomer such as the carboxy group-containing monomer.
- C 4-8 alkyl acrylate it may be 98% by weight or less (for example, less than 97% by weight).
- One type of C 4-8 alkyl acrylate can be used alone or two or more types can be used in combination. Suitable examples of C 4-8 alkyl acrylates include n-butyl acrylate (BA), n-heptyl acrylate (n-HpA) and 2-ethylhexyl acrylate (2EHA).
- the monomer component constituting the acrylic polymer includes BA.
- the proportion of BA in the monomer components of the acrylic polymer is, for example, more than 50% by weight, preferably 70% by weight or more, more preferably 80% by weight or more, still more preferably 85% by weight or more, particularly preferably 90% by weight. or more (for example, more than 90% by weight), and may be more than 92% by weight, more than 94% by weight, more than 95% by weight, or more than 96% by weight.
- a colorant such as a black colorant (e.g. carbon black) can be well dispersed in the adhesive layer, while maintaining good adhesive properties such as adhesive strength. be able to.
- the proportion of BA in the monomer component may be 99% by weight or less, or may be 97% by weight or less from the viewpoint of copolymerizing other copolymerizable monomers.
- the monomer component constituting the acrylic polymer contains heptyl acrylate.
- Acrylic polymers polymerized using monomer components containing heptyl acrylate are more flexible than polymers of other alkyl acrylates such as n-butyl acrylate (BA) and 2-ethylhexyl acrylate (2EHA).
- An adhesive containing a polymer can have a high 23°C tan ⁇ value, and can easily achieve both the 23°C storage modulus in the above range and the 23°C tan ⁇ in the above range.
- Heptyl acrylate is considered to be one of the most suitable monomer components for achieving both the above 23°C storage modulus and the above 23°C tan ⁇ .
- polymers of heptyl acrylate have excellent flexibility is not particularly limited, but polymers containing heptyl acrylate as a monomer unit have a low glass transition temperature and a This is thought to be because the space between them is relatively large.
- heptyl acrylates n-heptyl acrylate is preferred from the viewpoint of flexibility.
- Acrylic polymers synthesized containing n-heptyl acrylate as a monomer component are considered to have relatively long linear side chains, and therefore tend to have larger spaces between main chains.
- the proportion of heptyl acrylate in the monomer components of the acrylic polymer is, for example, 50% by weight or more (for example, more than 50% by weight) in some embodiments, suitably 70% by weight or more, preferably 80% by weight.
- the above is more preferably 85% by weight or more, further preferably 90% by weight or more (for example, more than 90% by weight), particularly preferably 92% by weight or more, may be 94% by weight or more, may be 95% by weight or more, and 96% by weight or more. It may be more than % by weight.
- the upper limit of the proportion of heptyl acrylate in the monomer component is 100% by weight, and may be 99% by weight or less, or may be 98% by weight or less. From the viewpoint of copolymerizing the carboxyl group-containing monomer and other monomers, in some embodiments, the proportion of heptyl acrylate in the monomer components is less than 97% by weight. In some preferred embodiments, the proportion of heptyl acrylate in the monomer component is 96% by weight or less, may be 95% by weight or less, and may be 94% by weight or less.
- the acrylic polymer may be copolymerized with an alkyl (meth)acrylate other than heptyl acrylate.
- alkyl (meth)acrylates other than heptyl acrylate include compounds represented by the above formula (1), and alkyl (meth)acrylates other than heptyl acrylate.
- Alkyl (meth)acrylates other than the above heptyl acrylate can be used alone or in combination of two or more.
- the proportion of heptyl acrylate in the total amount of alkyl (meth)acrylates contained in the monomer component is, for example, 50% by weight or more (specifically 50 to 100% by weight, for example, more than 50% by weight).
- 70% by weight or more, more preferably 80% by weight or more, still more preferably 90% by weight or more, particularly preferably 95% by weight or more may be 99% by weight or more, and may be 100% by weight. .
- the monomer component may include an alkyl (meth)acrylate having a biomass-derived alkyl group at the ester end (hereinafter also referred to as "biomass alkyl (meth)acrylate”).
- biomass alkyl (meth)acrylate having a biomass-derived alkyl group at the ester end
- biomass alkyl (meth)acrylate it is possible to suitably realize an acrylic pressure-sensitive adhesive that is designed to reduce dependence on fossil resource-based materials.
- the biomass alkyl (meth)acrylate is not particularly limited, and is, for example, an ester of a biomass-derived alkanol and a biomass-derived or non-biomass-derived (meth)acrylic acid.
- alkanols derived from biomass include biomass ethanol, alkanols derived from plant materials such as palm oil, palm kernel oil, coconut oil, and castor oil.
- the biomass-derived alkanol has three or more carbon atoms, the alkanol may be linear or branched.
- an ester of a biomass-derived alkanol and a non-biomass-derived (meth)acrylic acid is used as the biomass alkyl (meth)acrylate used in the synthesis of the acrylic polymer.
- biomass alkyl (meth)acrylate In such a biomass alkyl (meth)acrylate, the greater the number of carbon atoms in the alkanol, the greater the number ratio of biomass-derived carbon to the total number of carbons contained in the biomass alkyl (meth)acrylate, that is, the biomass carbon ratio of the alkyl (meth)acrylate. becomes higher. Therefore, in the above-mentioned biomass alkyl (meth)acrylate, it is desirable that the alkyl group derived from biomass has a large number of carbon atoms in order to reduce dependence on fossil resource materials.
- biomass-derived heptyl acrylate (biomass heptyl acrylate) is used as the heptyl acrylate.
- biomass heptyl acrylate is an ester of a biomass-derived alkanol and a biomass-derived or non-biomass-derived acrylic acid.
- an ester of a biomass-derived alkanol and a non-biomass-derived acrylic acid can be used. In such compounds, only the heptyl groups are derived from biomass.
- biomass-derived heptyl acrylate it is preferable to use biomass-derived n-heptyl acrylate (biomass n-heptyl acrylate).
- the proportion of biomass alkyl (meth)acrylate (preferably biomass heptyl acrylate) in the monomer components of the acrylic polymer is, for example, 50% by weight or more (for example, more than 50% by weight), preferably 70% by weight or more, more preferably 80% by weight or more, further preferably 85% by weight or more, particularly preferably 90% by weight or more, may be 92% by weight or more, may be 94% by weight or more, and may be 96% by weight or more. good.
- the proportion of biomass alkyl (meth)acrylate (preferably biomass heptyl acrylate) among the monomer components is less than 97% by weight, and in some embodiments may be 95% by weight or less, and may be 93% by weight or less. It may be 91% by weight or less.
- the monomer component of the acrylic polymer contains a carboxyl group-containing monomer.
- Carboxy group-containing monomers can improve cohesive force based on their polarity.
- the carboxy group can serve as a crosslinking point of the acrylic polymer.
- a carboxyl group-containing monomer it is easy to obtain an adhesive with improved storage modulus at 23°C.
- a carboxyl group-containing monomer better adhesion can be exhibited, for example, to adherends such as highly polar materials.
- the colorant can be easily dispersed in the layer and the adhesive properties can be improved. It can be maintained preferably.
- Carboxy group-containing monomers include, for example, acrylic acid (AA), methacrylic acid (MAA), carboxyethyl (meth)acrylate, carboxypentyl (meth)acrylate, crotonic acid, isocrotonic acid, and other ethylenically unsaturated monocarboxylic acids; maleic acid; acid, ethylenically unsaturated dicarboxylic acids such as itaconic acid and citraconic acid.
- the carboxy group-containing monomer may be a monomer having a metal salt (for example, an alkali metal salt) of a carboxy group. Carboxy group-containing monomers can be used alone or in combination of two or more.
- carboxy group-containing monomers include AA and MAA.
- AA is particularly preferred.
- the proportion of AA in the carboxy group-containing monomers is preferably 50% by weight or more, more preferably 70% by weight or more, and even more preferably 90% by weight or more. It is.
- the carboxy group-containing monomer consists essentially of AA.
- AA has a complex effect such as polarity based on its carboxyl group, role as a crosslinking point, Tg (106°C), etc., so AA improves the properties of the adhesive layer (23°C storage elasticity) in the carboxyl group-containing monomer disclosed herein. It is considered to be one of the most suitable monomer materials in achieving a well-balanced combination of adhesive properties such as adhesive strength and adhesion (gel fraction, etc.) and adhesive properties such as adhesive strength.
- the proportion of the carboxyl group-containing monomer in the monomer component of the acrylic polymer is not particularly limited, and may be 0.1% by weight or more, 0.5% by weight or more, 1% by weight or more, 2% by weight or more. It may be more than % by weight. In some preferred embodiments, the proportion of the carboxy group-containing monomer in the monomer component is more than 3% by weight (specifically more than 3.0% by weight), preferably 4.0% by weight or more, More preferably 4.5% by weight or more, still more preferably 5.0% by weight or more (for example, more than 5.0% by weight), particularly preferably 5.5% by weight or more, and 6.0% by weight or more. The content may be 6.5% by weight or more, or 7.0% by weight or more.
- the amount of the carboxyl group-containing monomer used By increasing the amount of the carboxyl group-containing monomer used, the cohesive force of the adhesive layer can be improved based on the action of the carboxyl group-containing monomer. Further, the amount of the carboxyl group-containing monomer is, for example, suitably 20% by weight or less of the monomer components, preferably 15% by weight or less, and more preferably 12% by weight or less. In some preferred embodiments, the amount of the carboxy group-containing monomer may be 10% by weight or less, 8% by weight or less, 6% by weight or less, or 5% by weight or less. By appropriately adjusting the amount of the carboxy group-containing monomer used within the above range, it is easy to obtain a pressure-sensitive adhesive having good adhesive properties.
- the acrylic polymer may be copolymerized with a functional group-containing monomer (any functional group-containing monomer) other than the carboxy group-containing monomer.
- a functional group-containing monomer any functional group-containing monomer
- optional functional group-containing monomers that can introduce functional groups that can serve as crosslinking base points into acrylic polymers or contribute to improving adhesive strength include hydroxyl group (OH group)-containing monomers (2-hydroxyethyl (meth)acrylate, 2-hydroxyethyl (meth)acrylate, 2- Hydroxyalkyl (meth)acrylates such as hydroxypropyl (meth)acrylate, 3-hydroxypropyl (meth)acrylate, 2-hydroxybutyl (meth)acrylate, 4-hydroxybutyl (meth)acrylate; polypropylene glycol mono(meth)acrylate, etc.
- OH group hydroxyl group
- 2-hydroxyethyl (meth)acrylate 2-hydroxyethyl (meth)acrylate
- acid anhydride group-containing monomers acid anhydride group-containing monomers, amide group-containing monomers ((meth)acrylamide, N,N-dimethyl(meth)acrylamide, etc.), amino group-containing monomers (aminoethyl (meth)acrylate, N,N-dimethylaminoethyl (meth)acrylate, etc.), epoxy group-containing monomers, cyano group-containing monomers, keto group-containing monomers, monomers with nitrogen atom-containing rings (N-vinyl-2-pyrrolidone, N-(meth)acryloylmorpholine, etc.), alkoxysilyl Examples include group-containing monomers, imide group-containing monomers, and the like. The above arbitrary functional group-containing monomers can be used alone or in combination of two or more.
- the content of the optional functional group-containing monomer in the monomer component is not particularly limited. From the viewpoint of appropriately exhibiting the effect of using the optional functional group-containing monomer, the content of the optional functional group-containing monomer in the monomer component can be, for example, 0.1% by weight or more, and 0.5% by weight or more. It is appropriate that the amount is 1% by weight or more.
- the monomer component of the acrylic polymer includes heptyl acrylate and a monomer containing a carboxyl group
- optional functional group-containing monomers in the monomer component may be used.
- the content of is suitably 40% by weight or less, preferably 20% by weight or less, and may be 10% by weight or less (for example, 5% by weight or less).
- the content of optional functional group-containing monomers in the monomer component is, for example, less than 3% by weight, may be less than 1% by weight, may be less than 0.5% by weight, and may be less than 0.3% by weight. % or less than 0.1% by weight.
- the technique disclosed herein can be preferably carried out in an embodiment in which the monomer component of the acrylic polymer does not substantially contain any functional group-containing monomer.
- the monomer component does not substantially contain monomer A (for example, the above-mentioned optional functional group-containing monomer), it means that the monomer A is not used at least intentionally, and the monomer component is, for example, Unintentional inclusion of about 0.01% by weight or less is acceptable.
- a hydroxyl group-containing monomer may be used as the optional functional group-containing monomer.
- the content of the hydroxyl group-containing monomer in the monomer components is suitably about 10% by weight or less (for example, 0.001 to 10% by weight), preferably about 5% by weight or less, and more preferably about 5% by weight or less. It is 2% by weight or less.
- the content of hydroxyl-containing monomer in the monomer component may be less than 1% by weight, less than 0.5% by weight, less than 0.3% by weight, 0.1% by weight, etc. % or less than 0.01% by weight.
- the monomer component of the acrylic polymer may be substantially free of hydroxyl group-containing monomers. In the technology disclosed herein, desired characteristics and effects can be preferably achieved with a composition in which the amount of the hydroxyl group-containing monomer used is limited or is not used.
- the ratio of the carboxy group-containing monomer to the total functional group-containing monomers (total functional group-containing monomers including the carboxy group-containing monomer) used as a copolymerization component of the acrylic polymer is determined by the effect of copolymerizing the carboxy group-containing monomer.
- the content is suitably 30% by weight or more, preferably 50% by weight or more, more preferably 70% by weight or more, even more preferably 80% by weight or more, particularly preferably 90% by weight or more, such as It may be 95% by weight or more, 97% by weight or more, 98% by weight or more, or 99% by weight or more (for example, 99.9% by weight or more).
- the upper limit of the proportion of the carboxy group-containing monomer to the total of the functional group-containing monomers is 100% by weight, and may be, for example, 95% by weight or less.
- the monomer components constituting the acrylic polymer may contain copolymerization components other than the above-mentioned functional group-containing monomers for the purpose of improving cohesive force and the like.
- copolymerizable components include vinyl ester monomers such as vinyl acetate; aromatic vinyl compounds such as styrene; cycloalkyl (meth)acrylate, cyclopentyl (meth)acrylate, and isobornyl (meth)acrylate; ) acrylates; aryl (meth)acrylates (e.g. phenyl (meth)acrylate), aryloxyalkyl (meth)acrylates (e.g.
- Aromatic ring-containing (meth)acrylate Olefinic monomer; Chlorine-containing monomer; Isocyanate group-containing monomer such as 2-(meth)acryloyloxyethyl isocyanate; Alkoxy such as methoxyethyl (meth)acrylate and ethoxyethyl (meth)acrylate Group-containing monomers; vinyl ether monomers such as methyl vinyl ether and ethyl vinyl ether; and the like.
- the other copolymerization components mentioned above can be used alone or in combination of two or more.
- the amount of such other copolymerized components is not particularly limited as long as it can be selected as appropriate depending on the purpose and use, but from the viewpoint of appropriately exhibiting the effects of use, it is appropriate to set it to 0.05% by weight or more. , 0.5% by weight or more.
- the content of other copolymer components in the monomer component is 20% by weight or less, so that the adhesive properties based on the essential monomer components can be suitably exhibited. From this point of view, it is preferably 10% by weight or less, more preferably 8% by weight or less, still more preferably less than 5% by weight, for example, it may be less than 3% by weight, and may be less than 1% by weight.
- the technology disclosed herein can also be preferably practiced in an embodiment in which the monomer component does not substantially contain other copolymer components.
- Acrylic polymers are polyfunctional polymers that have at least two polymerizable functional groups (typically radically polymerizable functional groups) having unsaturated double bonds such as (meth)acryloyl groups and vinyl groups as other monomer components. It may also contain monomers. By using a polyfunctional monomer as a monomer component, the cohesive force of the adhesive layer can be increased. Polyfunctional monomers can be used as crosslinking agents.
- the polyfunctional monomer is not particularly limited, and includes, for example, 1,6-hexanediol di(meth)acrylate, trimethylolpropane tri(meth)acrylate, dipentaerythritol hexa(meth)acrylate, and neopentyl glycol di(meth)acrylate. etc.
- One type of polyfunctional monomer can be used alone or two or more types can be used in combination.
- the amount of the polyfunctional monomer used is not particularly limited, and can be appropriately set so that the intended use of the polyfunctional monomer is achieved.
- the amount of the polyfunctional monomer used can be about 3% by weight or less of the monomer components, preferably about 2% by weight or less, and more preferably about 1% by weight or less (for example, about 0.5% by weight or less).
- the lower limit of the amount used when using a polyfunctional monomer is not particularly limited, as long as it is greater than 0% by weight.
- the effect of using the polyfunctional monomer can be appropriately exhibited by setting the amount of the polyfunctional monomer to be approximately 0.001% by weight or more (for example, approximately 0.01% by weight or more) of the monomer components.
- the acrylic polymer is an acrylic polymer synthesized using a monomer component consisting essentially of heptyl acrylate (preferably n-heptyl acrylate) and a carboxy group-containing monomer (preferably acrylic acid). It will be done. According to the above monomer composition, the effects of heptyl acrylate and the carboxy group-containing monomer are effectively exhibited, and the prescribed storage modulus at 23°C and tan ⁇ at 23°C are both achieved, thereby achieving a high degree of suppression of fine uneven deformation. can do.
- heptyl acrylate preferably n-heptyl acrylate
- carboxy group-containing monomer preferably acrylic acid
- the total proportion of heptyl acrylate and the carboxyl group-containing monomer in the monomer components is suitably 90% by weight or more (90 to 100% by weight), preferably 95% by weight or more, more preferably 99% by weight or more. % by weight or more, more preferably more than 99.5% by weight, particularly preferably more than 99.9% by weight (for example, more than 99.99% by weight), and the total proportion of heptyl acrylate and the carboxy group-containing monomer in the monomer components may be 100% by weight.
- biomass carbon ratio of the monomer component constituting the acrylic polymer may be, for example, 1% or more, suitably 10% or more, preferably 30% or more, and more preferably is 50% or more (for example, more than 50%), may be 70% or more, may be 80% or more, or may be 90% to 100%.
- the copolymer composition of the acrylic polymer is designed such that the glass transition temperature (Tg) of the polymer is approximately -15°C or lower (for example, approximately -70°C or more and -15°C or less).
- Tg glass transition temperature
- the Tg of the acrylic polymer refers to the Tg determined by the Fox equation based on the composition of monomer components used in the synthesis of the polymer.
- the Fox equation as shown below, is a relational equation between Tg of a copolymer and the glass transition temperature Tgi of a homopolymer obtained by homopolymerizing each of the monomers constituting the copolymer.
- Tg is the glass transition temperature of the copolymer (unit: K)
- Wi is the weight fraction of monomer i in the copolymer (copolymerization ratio on a weight basis)
- Tgi is the weight fraction of monomer i in the copolymer. Represents the glass transition temperature (unit: K) of a homopolymer.
- the glass transition temperature of the homopolymer used to calculate Tg the values listed in publicly known materials, specifically "Polymer Handbook” (3rd edition, John Wiley & Sons, Inc., 1989), shall be used. .
- the highest value is adopted. If it is not described in the above Polymer Handbook, the value obtained by the measurement method described in JP-A No. 2007-51271 shall be used.
- the Tg of the acrylic polymer is approximately -25°C or lower, preferably approximately -35°C or lower. , more preferably about -40°C or lower.
- the Tg of the acrylic polymer is, for example, about -70°C or higher, may be about -65°C or higher, may be about -60°C or higher, or even about -55°C or higher. good.
- the technology disclosed herein can be preferably carried out in an embodiment in which the Tg of the acrylic polymer is about -65°C or more and -35°C or less (for example, about -55°C or more and -40°C or less).
- the Tg of the acrylic polymer can be adjusted by appropriately changing the monomer composition (that is, the type and usage ratio of monomers used to synthesize the polymer).
- the method for obtaining the acrylic polymer is not particularly limited, and various polymerization methods known as methods for synthesizing acrylic polymers such as solution polymerization, emulsion polymerization, bulk polymerization, suspension polymerization, and photopolymerization may be used. may be adopted as appropriate.
- a solution polymerization method can be preferably employed.
- a monomer supply method when performing solution polymerization a batch charging method in which all monomer raw materials are supplied at once, a continuous supply (dropping) method, a divided supply (dropping) method, etc. can be appropriately adopted.
- the polymerization temperature can be selected as appropriate depending on the type of monomer and solvent used, the type of polymerization initiator, etc., and is, for example, about 20°C to 170°C (typically about 40°C to 140°C). Can be done.
- the solvent (polymerization solvent) used for solution polymerization can be appropriately selected from conventionally known organic solvents.
- aromatic compounds typically aromatic hydrocarbons
- acetate esters such as ethyl acetate
- aliphatic or alicyclic hydrocarbons such as hexane and cyclohexane
- 1,2-dichloroethane, etc. halogenated alkanes lower alcohols such as isopropyl alcohol (for example, monohydric alcohols having 1 to 4 carbon atoms); ethers such as tert-butyl methyl ether; ketones such as methyl ethyl ketone; etc.
- Any one type of solvent or a mixed solvent of two or more types can be used.
- the initiator used for polymerization can be appropriately selected from conventionally known polymerization initiators depending on the type of polymerization method.
- one or more azo polymerization initiators such as 2,2'-azobisisobutyronitrile (AIBN) can be preferably used.
- Other examples of polymerization initiators include persulfates such as potassium persulfate; peroxide initiators such as benzoyl peroxide (BPO) and hydrogen peroxide; substituted ethane initiators such as phenyl-substituted ethane; aromatic carbonyl compounds; and the like.
- Still another example of the polymerization initiator is a redox initiator using a combination of a peroxide and a reducing agent.
- Such polymerization initiators can be used alone or in combination of two or more.
- the amount of the polymerization initiator used may be any normal amount, for example, approximately 0.005 to 1 part by weight (typically approximately 0.01 to 1 part by weight) per 100 parts by weight of all monomer components. degree).
- the weight average molecular weight (Mw) of the acrylic polymer is not particularly limited, and an acrylic polymer having an appropriate Mw that can satisfy both the above-mentioned 23° C. storage modulus and 23° C. tan ⁇ is used.
- the Mw of the acrylic polymer can range from approximately 10 ⁇ 10 4 to 500 ⁇ 10 4 .
- the Mw of the base polymer may be about 20 ⁇ 10 4 or more, about 30 ⁇ 10 4 or more, about 40 ⁇ 10 4 or more, or about 50 ⁇ 10 4 or more.
- the Mw of the acrylic polymer may be greater than 600,000, greater than 650,000, suitably greater than 700,000, and may be greater than 750,000.
- the Mw of the acrylic polymer is 800,000 or more, may be 850,000 or more, may be 900,000 or more, may be 1 million or more (for example, more than 1 million), or may be 1.2 million or more. good.
- the viscosity can be easily maintained at a low level, so that synthesis of a high molecular weight product is good, and an acrylic polymer having the above Mw can be easily obtained.
- the Mw of the acrylic polymer is usually approximately 3 million or less, preferably 2.5 million or less, and more preferably 2 million or less. , more preferably 1.8 million or less, may be 1.5 million or less, or may be 1.3 million or less.
- the Mw of the acrylic polymer may be 1.1 million or less, 1 million or less, 950,000 or less, or 900,000 or less. In some other preferred embodiments, the Mw of the acrylic polymer is 800,000 or less, may be 600,000 or less, may be less than 500,000, or may be 450,000 or less. By appropriately limiting the Mw of the acrylic polymer, the 23°C tan ⁇ tends to improve.
- the Mw of the acrylic polymer can be measured by gel permeation chromatography (GPC) and determined as a value in terms of standard polystyrene. Specifically, it can be determined by measuring under the following conditions using a GPC measurement device with the trade name "HLC-8220GPC" (manufactured by Tosoh Corporation). The same applies to the embodiments described later.
- GPC gel permeation chromatography
- the colored adhesive layer typically contains a colorant.
- the adhesive layer is colored and can have desired optical properties (light transmittance, etc.), hiding properties, design properties, and color.
- the colorant may be, for example, black, gray, white, red, blue, yellow, green, yellow-green, orange, purple, gold, silver, pearlescent, or the like.
- the above-mentioned coloring agent may be contained in the adhesive layer, typically in a dispersed state (or may be in a dissolved state) in the constituent material of the adhesive layer.
- the colorant conventionally known pigments and dyes can be used. Examples of pigments include inorganic pigments and organic pigments.
- One type of colorant can be used alone or two or more types can be used in combination. Note that when the double-sided pressure-sensitive adhesive sheet disclosed herein includes a non-colored pressure-sensitive adhesive layer, the pressure-sensitive adhesive layer does not substantially contain a colorant.
- the coloring agent is not particularly limited, and is, for example, a component that can absorb and attenuate light traveling through the adhesive layer, and by including the colorant in the adhesive layer, the light transmittance of the adhesive layer can be increased. (therefore also referred to as a "light transmittance reducing component").
- a coloring agent hereinafter also referred to as "first coloring agent”
- a black coloring agent can be preferably used because it is possible to efficiently adjust hiding properties and light blocking properties by using a small amount.
- the black colorant examples include carbon black, graphite, aniline black, perylene black, cyanine black, titanium black, inorganic pigment hematite, activated carbon, molybdenum disulfide, chromium complex, anthraquinone colorant, and the like.
- the black coloring agent can be used alone or in an appropriate combination of two or more.
- the adhesive layer contains carbon black particles as a colorant (first colorant).
- carbon black particles those generally referred to as carbon black (furnace black, channel black, acetylene black, thermal black, lamp black, pine smoke, etc.) can be used without particular limitation.
- surface-modified carbon black particles having functional groups such as carboxy groups, amino groups, sulfonic acid groups, and silicon-containing groups (eg, alkoxysilyl groups, alkylsilyl groups) as carbon black particles.
- Such surface-modified carbon black particles are also called self-dispersing carbon blacks, and can eliminate the need for adding a dispersant or reduce the amount added.
- the above carbon black particles can be used alone or in combination of two or more.
- a particulate colorant can be preferably used because the light transmittance of the adhesive layer can be efficiently adjusted by using a small amount.
- a colorant e.g., a particulate black colorant such as carbon black
- the average particle size is, for example, about 50 nm or more, may be about 100 nm or more, may be about 150 nm or more, may be about 200 nm or more, may be about 300 nm or more, or may be about 350 nm or more.
- the upper limit of the average particle size of the colorant is not particularly limited, and may be, for example, about 3000 nm or less, or may be about 1000 nm or less. From the viewpoint of reducing the light transmittance, the average particle size of the colorant is suitably about 500 nm or less, may be about 300 nm or less, or may be 200 nm or less.
- the average particle size of the colorant in this specification refers to the volume average particle size, and specifically, the integrated value of 50% in the particle size distribution measured based on a particle size distribution measuring device based on a laser scattering/diffraction method. refers to the particle size (50% volume average particle size; hereinafter sometimes abbreviated as D50 ).
- the measuring device for example, the product name "Microtrac MT3000II” manufactured by Microtrac Bell Co., Ltd. or its equivalent product can be used.
- the form in which the colorant preferably a black colorant such as carbon black particles
- the colorant preferably a black colorant such as carbon black particles
- a colorant such as carbon black particles may be added to the adhesive composition in the form of a dispersion in which the particles are dispersed in a dispersion medium.
- the dispersion medium constituting the dispersion liquid is not particularly limited, and may include water (ion exchange water, reverse osmosis water, distilled water, etc.), various organic solvents (alcohols such as ethanol; ketones such as acetone; butyl cellosolve, propylene glycol monomethyl Examples include ethers such as ether acetate; esters such as ethyl acetate; aromatic hydrocarbons such as toluene; mixed solvents thereof), and aqueous mixed solvents of water and the above organic solvents.
- the above-mentioned dispersion liquid may contain the above-mentioned dispersant.
- the adhesive composition contains a colorant (preferably a black colorant such as carbon black particles) and may also contain a dispersant.
- the content of the first colorant (preferably a black colorant such as carbon black particles) is determined based on the adherend hiding ability and optical properties (light transmittance, etc.). It is appropriately set in consideration of adjustment, required adhesive properties, etc., and is not limited to a specific range. Further, the content of the first colorant may vary depending on the type of adhesive, the shape and particle size of the first colorant, compatibility with the adhesive, and the like.
- the content of the first colorant in the adhesive layer is suitably approximately 0.01% by weight or more, may be 0.05% by weight or more, may be 0.1% by weight or more, and From the viewpoint of concealing properties, the content is preferably about 0.3% by weight or more, more preferably about 0.5% by weight or more. In some embodiments, the content of the first colorant is suitably about 1% by weight or more (for example, more than 1% by weight), and may be about 2% by weight or more. Further, in an embodiment in which the adhesive layer contains the first colorant or in an embodiment in which the adhesive layer does not contain the first colorant, the content of the first colorant (preferably a black colorant such as carbon black particles) is approximately 30% by weight.
- the content of the first colorant (preferably a black colorant such as carbon black particles) may be about 2% by weight or less, about 1% by weight or less, or about 0% by weight. The content may be .5% by weight or less (for example, 0.3% by weight or less).
- adhesive properties such as adhesive strength tend to be easily maintained.
- the adhesive layer may be implemented in an embodiment including a second colorant (for example, a metal oxide described below) as described below as a colorant.
- a second colorant is defined as a different colorant than the first colorant.
- the adhesive layer may include a second colorant and be substantially free of the first colorant described above.
- the second colorant is not particularly limited, but for example, like the first adhesive, it may be a component that reduces the light transmittance of the adhesive layer, or it may be a component that reduces the light transmittance of the adhesive layer. It may also be a component that can reduce the amount of light. Further, the second colorant may be a component that imparts a different color or hue from the first colorant. Such a second colorant may be selected from, for example, a white colorant or a gray colorant.
- the second colorant may be one or more selected from inorganic materials (eg, metals, metal compounds), organic materials, and organic-inorganic composites.
- the second colorant include titanium oxide (rutile titanium dioxide, anatase titanium dioxide, etc.), zinc oxide, cerium oxide, aluminum oxide, silicon oxide, zirconium oxide, magnesium oxide, calcium oxide, Metal oxides such as tin, barium oxide, cesium oxide, yttrium oxide; carbonate compounds such as magnesium carbonate, calcium carbonate (light calcium carbonate, heavy calcium carbonate, etc.), barium carbonate, zinc carbonate; aluminum hydroxide, calcium hydroxide , hydroxides such as magnesium hydroxide, zinc hydroxide; silicate compounds such as aluminum silicate, magnesium silicate, calcium silicate; barium sulfate, calcium sulfate, barium stearate, zinc white, zinc sulfide, talc, clay, kaolin, phosphoric acid Inorganic materials such as titanium, mica, gypsum, white carbon, diatomaceous earth, bentonite, lithopone, zeolite, sericite, hydrated halloysite, etc., acrylic resin
- the adhesive layer contains a metal oxide as a second colorant.
- a metal oxide as a second colorant.
- the metal oxide can be selected from the materials mentioned above. Suitable examples include titanium oxide, zinc oxide, cerium oxide, aluminum oxide, silicon oxide, zirconium oxide, magnesium oxide, and calcium oxide. Among them, titanium oxide, silicon oxide, and zirconium oxide are preferred, and titanium oxide is particularly preferred. preferable.
- One kind of metal oxide can be used alone or two or more kinds can be used in combination.
- the average particle size of the second colorant (for example, a white colorant, preferably metal oxide particles) is not particularly limited. Depending on the thickness of the adhesive layer, the type of adhesive, etc., particles of an appropriate size that can achieve desired optical properties (light transmittance, etc.) can be used.
- the average particle size of the second colorant can be, for example, about 1 nm or more, and suitably about 5 nm or more. From the viewpoints of compatibility, handleability, etc., the average particle size of the second colorant is preferably about 10 nm or more, about 20 nm or more, or about 30 nm or more.
- the upper limit of the average particle diameter is, for example, approximately 300 nm or less, preferably less than 100 nm (for example, 90 nm or less), more preferably approximately 70 nm or less, and still more preferably approximately 50 nm or less. , approximately 35 nm or less (for example, approximately 25 nm or less).
- the content of the second colorant (for example, a white colorant, preferably a metal oxide) in the adhesive layer is determined by the effect of containing the second colorant; It is appropriately set in consideration of the required adhesive properties, etc., and is not limited to a specific range. Further, the content of the second colorant may vary depending on the type of adhesive, the shape and particle size of the second colorant, compatibility with the adhesive, and the like. The content of the second colorant in the adhesive layer is suitably about 1% by weight or more, preferably about 2% by weight or more, more preferably about 2% by weight or more, from the viewpoint of effectively obtaining the effect of containing the second colorant.
- the adhesive layer contains the second colorant or in embodiments in which it does not contain the second colorant
- the content of the second colorant in the adhesive layer depends on its compatibility with the adhesive component, adhesive strength, and durability. From the viewpoint of maintaining adhesive properties such as impact resistance, it can be about 30% by weight or less, suitably about 25% by weight or less, may be about 20% by weight or less, and even about 15% by weight or less. Generally, it may be about 12% by weight or less, about 10% by weight or less, or about 8% by weight or less.
- the ratio of the amount C1 of the first colorant to the amount C2 of the second colorant depends on the intended adherend hiding property and the optical It is appropriately set to achieve adjustment of characteristics (light transmittance, etc.), design, and color, and is not limited to a specific range.
- the weight ratio (C2/ C1) is approximately 0.01 or more, suitably 0.1 or more, preferably 1 or more (for example, more than 1), may be 10 or more, may be 30 or more, and is 50 or more (for example, 70 or more). But that's fine.
- the weight ratio (C2/C1) is approximately 1000 or less, suitably 500 or less, preferably 300 or less, may be 100 or less, may be 80 or less, It may be 60 or less.
- the first colorant is a black colorant, there is a tendency for the covering property to be improved.
- the content of colorants other than the black colorant and the metal oxide is not particularly limited. For example, it may be less than 30% by weight of the entire adhesive layer, preferably less than 10% by weight, and may be less than 5.0% by weight, and less than 3.0% by weight (for example, 2.0% by weight). or even less than 1% by weight).
- the technology disclosed herein can be implemented in an embodiment that includes an adhesive layer that does not substantially contain a black colorant and a colorant other than a metal oxide.
- substantially not included means not intentionally added, and for example, the content in the adhesive layer is 0.3% by weight or less (for example, 0.1% by weight or less, (typically 0.01% by weight or less).
- the colorant from the viewpoint of compatibility with the adhesive component, it is possible to use the material (particulate colorant) exemplified as the colorant described above that has been surface-treated with a surface treatment agent.
- a surface treatment agent an appropriate treatment can be selected depending on the type of core particles, the type of dispersion medium, etc., so it is not limited to a specific treatment.
- the adhesive composition disclosed herein may contain a component that contributes to improving the dispersibility of the colorant.
- Such dispersibility-enhancing components can be, for example, polymers, oligomers, liquid resins, surfactants (anionic, cationic, nonionic, amphoteric surfactants), and the like.
- the dispersibility improving components can be used alone or in combination of two or more. It is preferable that the dispersibility improving component is dissolved in the adhesive composition.
- the oligomer is, for example, a low molecular weight polymer of a monomer component containing one or more of the acrylic monomers exemplified above (for example, Mw is less than about 10 x 10 4 , preferably less than 5 x 10 4 acrylic oligomers).
- the liquid resin may be, for example, a tackifying resin (typically a rosin-based, terpene-based, or hydrocarbon-based tackifying resin, such as a hydrogenated rosin) having a softening point of approximately 50°C or lower, more preferably approximately 40°C or lower. methyl ester, etc.).
- a dispersibility improving component can suppress uneven dispersion of a colorant (for example, a particulate black colorant such as carbon black) and, in turn, suppress uneven coloring of the adhesive layer. Therefore, it is possible to form an adhesive layer with better appearance quality.
- the form of addition of the dispersibility improving component is not particularly limited, and it may be included in a liquid containing a colorant (for example, a black colorant such as carbon black particles) before being added to the adhesive composition, or it may be added to the liquid containing a colorant (for example, a black colorant such as carbon black particles) before being added to the adhesive composition. It may be supplied into the product at the same time as the colorant, or before or after the addition of the colorant.
- a colorant for example, a black colorant such as carbon black particles
- the content of the dispersibility-improving component is not particularly limited, and from the viewpoint of suppressing the influence on adhesive properties (for example, a decrease in cohesiveness), the content of the dispersibility-improving component is about 20% by weight or less (preferably about 10% by weight or less, more preferably about 10% by weight or less) of the entire adhesive layer.
- the content is preferably 7% by weight or less, for example approximately 5% by weight or less).
- the content of the dispersibility-enhancing component can be about 10 times or less (preferably about 5 times or less, for example about 3 times or less) the weight of the colorant.
- the content of the dispersibility improving component should be approximately 0.2% by weight or more (typically approximately 0.5% by weight or more, preferably approximately 1% by weight) based on the entire adhesive layer. % by weight or more).
- the content of the dispersibility improving component can be about 0.2 times or more (preferably about 0.5 times or more, for example, 1 time or more) the weight of the colorant.
- the content of the colorant in the adhesive layer depends on the intended adherend hiding ability, optical properties (light transmittance, etc.), It is appropriately set in consideration of design, color, etc., required adhesive properties, etc., and is not limited to a specific range.
- the content of the colorant in the pressure-sensitive adhesive layer is approximately 0.1% by weight or more, suitably approximately 0.5% by weight or more, and preferably approximately 1% by weight or more from the viewpoint of hideability of adherends, etc. , more preferably about 1.5% by weight or more, still more preferably about 2% by weight or more.
- the content of the colorant in the adhesive layer is suitably about 3% by weight or more, may be about 5% by weight or more, or may be about 7% by weight or more.
- the content of the colorant in the adhesive layer can be approximately 30% by weight or less from the viewpoint of compatibility with the adhesive component and maintenance of adhesive properties such as adhesive strength and impact resistance, and is usually approximately 30% by weight or less. Appropriately it is 20% by weight or less, it may be about 15% by weight or less, it may be about 10% by weight or less, it may be about 8% by weight or less, it may be about 6% by weight or less, it may be about 4% by weight or less. good.
- the adhesive layer includes a tackifying resin. Adhesive strength can be improved by using a tackifying resin. According to the technology disclosed herein, the adhesive layer has a composition containing a tackifying resin and has predetermined viscoelastic properties (specifically, 23°C storage modulus and 23°C tan ⁇ ) and gel fraction. obtain. Although not particularly limited, the effect of using a tackifying resin can be effectively exhibited in a composition containing a high molecular weight acrylic polymer.
- the tackifier resin is not particularly limited and includes, for example, rosin-based tackifier resin, terpene-based tackifier resin, hydrocarbon-based tackifier resin, epoxy-based tackifier resin, polyamide-based tackifier resin, elastomer-based tackifier resin, Various tackifying resins such as phenolic tackifying resins and ketone tackifying resins can be used. Such tackifying resins can be used alone or in combination of two or more.
- rosin-based tackifying resins include unmodified rosin (raw rosin) such as gum rosin, wood rosin, and tall oil rosin; Hydrogenated rosin, disproportionated rosin, polymerized rosin, other chemically modified rosin, etc. (the same applies hereinafter); and other various rosin derivatives.
- unmodified rosin raw rosin
- Hydrogenated rosin disproportionated rosin
- polymerized rosin other chemically modified rosin, etc.
- other various rosin derivatives include rosins such as those obtained by esterifying unmodified rosin with alcohols (i.e., esterified products of rosin), and those obtained by esterifying modified rosin with alcohols (i.e., esterified products of modified rosin).
- Esters Unsaturated fatty acid-modified rosins, which are unmodified rosin or modified rosin modified with unsaturated fatty acids; Unsaturated fatty acid-modified rosin esters, which are rosin esters modified with unsaturated fatty acids; Unmodified rosin, modified rosin, unsaturated Rosin alcohols obtained by reducing the carboxyl group in fatty acid-modified rosins or unsaturated fatty acid-modified rosin esters; metal salts of rosins (especially rosin esters) such as unmodified rosin, modified rosin, and various rosin derivatives; rosins; Examples include rosin phenol resins obtained by adding phenol to (unmodified rosin, modified rosin, various rosin derivatives, etc.) with an acid catalyst and thermally polymerizing them. Among them, rosin ester is preferred.
- rosin esters include esters of unmodified rosin or modified rosin (hydrogenated rosin, disproportionated rosin, polymerized rosin, etc.), such as methyl ester, triethylene glycol ester, glycerin ester. , pentaerythritol ester and the like.
- terpene-based tackifying resins examples include terpene resins such as ⁇ -pinene polymer, ⁇ -pinene polymer, and dipentene polymer; modified terpene resins; and the like.
- modified terpene resin is terpene phenol resin.
- Terpene phenol resin refers to a polymer containing terpene residues and phenol residues, and includes copolymers of terpenes and phenol compounds (terpene-phenol copolymer resins), and homopolymers or copolymers of terpenes. This concept includes both phenol-modified products (phenol-modified terpene resins). Specific examples of terpenes constituting such terpene phenol resin include monoterpenes such as ⁇ -pinene, ⁇ -pinene, and limonene (including d-form, l-form, and d/l-form (dipentene)); can be mentioned.
- the hydrogenated terpene phenol resin refers to a hydrogenated terpene phenol resin having a structure obtained by hydrogenating such a terpene phenol resin. Sometimes called hydrogenated terpene phenolic resin.
- hydrocarbon-based tackifier resins examples include aliphatic (C5-based) petroleum resins, aromatic (C9-based) petroleum resins, aliphatic/aromatic copolymerized (C5/C9-based) petroleum resins, and Hydrogenated substances (e.g., alicyclic petroleum resins obtained by hydrogenating aromatic petroleum resins), various modified products thereof (e.g., maleic anhydride modified products), coumaron-based resins, coumaron-indene-based resins Examples include various hydrocarbon resins such as.
- the total proportion of the rosin-based tackifying resin and the terpene-based tackifying resin in the entire tackifying resin contained in the adhesive layer is, for example, approximately more than 50% by weight (more than 50% by weight and not more than 100% by weight). ), and may be about 70% by weight or more, about 80% by weight or more, about 90% by weight or more, about 95% by weight or more, or about 99% by weight or more.
- Some preferred embodiments include embodiments in which the tackifying resin contains one or more terpene phenol resins.
- the technology disclosed herein can be preferably implemented, for example, in an embodiment in which about 25% by weight or more (more preferably about 30% by weight or more) of the total amount of tackifying resin is a terpene phenol resin.
- the proportion of the terpene phenol resin in the total amount of tackifying resin may be approximately 50% by weight or more, approximately 70% by weight or more, approximately 80% by weight or more, or approximately 90% by weight or more.
- Substantially all of the tackifying resin (for example, about 95% to 100% by weight, and even about 99% to 100% by weight) may be a terpene phenol resin.
- the content of the terpene phenol resin in the adhesive layer is not particularly limited as long as it satisfies the desired properties (viscoelastic properties, etc.).
- the content of the terpene phenol resin is usually about 1 part by weight or more, and suitably about 5 parts by weight or more, based on 100 parts by weight of the acrylic polymer, from the viewpoint of improving adhesive strength.
- the amount is preferably about 8 parts by weight or more, more preferably about 10 parts by weight or more, and even more preferably about 12 parts by weight or more (for example, 15 parts by weight or more).
- the content of the terpene phenol resin in the adhesive layer is, for example, 70 parts by weight or less, may be 60 parts by weight or less, and may be 50 parts by weight or less, based on 100 parts by weight of the acrylic polymer.
- the amount may be less than 40 parts by weight, or less than 30 parts by weight.
- the content of the terpene phenol resin is less than 30 parts by weight, more preferably 25 parts by weight or less, and even more preferably 22 parts by weight, from the viewpoint of improving the uneven deformation relaxation property of the adhesive. or less, and may be 20 parts by weight or less.
- the softening point of the tackifying resin is not particularly limited. From the viewpoint of improving cohesive force, a tackifier resin having a softening point (softening temperature) of about 80° C. or higher can be preferably used. The softening point of the tackifying resin may be approximately 100°C or higher, or approximately 110°C or higher. Further, from the viewpoint of adhesion to the adherend, a tackifier resin having a softening point of approximately 200° C. or lower (more preferably approximately 180° C. or lower) may be preferably used. In some embodiments, the softening point of the tackifying resin may be less than 160°C, and may be less than 150°C.
- the softening point of the tackifier resin in this specification is defined as a value measured based on the softening point test method (ring and ball method) specified in JIS K5902 and JIS K2207. Specifically, the sample is melted as quickly as possible at the lowest possible temperature, and the sample is carefully filled into a ring placed on a flat metal plate, taking care not to form bubbles. After it has cooled down, use a slightly heated knife to cut off the raised part from the plane including the top of the ring.
- a supporter (ring stand) is placed in a glass container (heating bath) with a diameter of 85 mm or more and a height of 127 mm or more, and glycerin is poured into the container to a depth of 90 mm or more.
- the steel ball (diameter 9.5 mm, weight 3.5 g) and the ring filled with the sample were immersed in glycerin without coming into contact with each other, and the temperature of the glycerin was maintained at 20°C plus or minus 5°C for 15 minutes. .
- a steel ball is then placed in the center of the surface of the sample in the ring and placed in position on the support.
- thermometer place a thermometer, set the center of the mercury bulb of the thermometer at the same height as the center of the ring, and heat the container.
- the flame of the Bunsen burner used for heating should be halfway between the center of the bottom of the container and the edge to ensure even heating. Note that the rate at which the bath temperature increases after heating starts and reaches 40°C must be 5.0 plus or minus 0.5°C per minute.
- the sample gradually softens and flows down from the ring, and the temperature at which it finally touches the bottom plate is read, and this is taken as the softening point.
- the softening point is measured at two or more points at the same time, and the average value is used.
- the tackifying resin is a tackifying resin T L having a softening point of less than 150°C.
- the softening point of the tackifier resin T L is less than 140°C, more preferably less than 130°C, even more preferably less than 120°C, and may be 110°C or less, and has a softening point of 100°C or less.
- the temperature may be lower than or equal to 90°C.
- the lower limit of the softening point of the tackifier resin T L is not particularly limited.
- the softening point of the tackifier resin T L may be approximately 50°C or higher, 60°C or higher, 70°C or higher, or 80°C from the viewpoint of exhibiting appropriate cohesive force. or higher, 90°C or higher, 100°C or higher, or 110°C or higher.
- the tackifier resin T L one type suitably selected from among the tackifier resins exemplified above having a softening point of less than 150°C can be used alone or in combination of two or more types.
- the tackifying resin T L preferably includes at least one selected from rosin-based tackifying resins and terpene-based tackifying resins.
- the tackifying resin T L may contain one type of rosin-based tackifying resin alone, or may contain a combination of two or more types of rosin-based tackifying resin.
- the tackifying resin T L may contain one type of terpene-based tackifying resin (eg, terpene phenol resin) alone, or may contain a combination of two or more types of terpene-based tackifying resin.
- terpene-based tackifying resin eg, terpene phenol resin
- the proportion of the terpene-based tackifying resin (e.g., terpene phenol resin) in the entire tackifying resin T L can be, for example, more than about 50% by weight, and may be about 65% by weight or more, The content may be approximately 75% by weight or more, 85% by weight or more, or 95% by weight or more.
- the technology disclosed herein is an embodiment in which substantially all of the tackifier resin T L (for example, approximately 97% by weight or more, or 99% by weight or more, and may be 100% by weight) is a terpene-based tackifier resin. It can be preferably carried out.
- examples of rosin-based tackifier resins that can be preferably employed as the tackifier resin T L include rosin esters such as unmodified rosin esters and modified rosin esters.
- a suitable example of the modified rosin ester is a hydrogenated rosin ester.
- esters of unmodified rosin or modified rosin eg, hydrogenated rosin
- rosin esters such as methyl ester, glycerin ester, etc.
- the tackifying resin T L may include a hydrogenated rosin ester.
- the tackifying resin T L may include a non-hydrogenated rosin ester.
- non-hydrogenated rosin ester is a concept that comprehensively refers to rosin esters other than hydrogenated rosin esters mentioned above. Examples of non-hydrogenated rosin esters include unmodified rosin esters, disproportionated rosin esters and polymerized rosin esters.
- the tackifier resin T L may contain a combination of a hydrogenated rosin ester and a non-hydrogenated rosin ester as rosin esters, or may contain only one or more hydrogenated rosin esters. It may contain only one species or two or more non-hydrogenated rosin esters. In some embodiments, only one or more hydrogenated rosin esters may be used as the rosin esters contained in the tackifier resin T L.
- tackifying resin T L for example, a tackifying resin having a softening point of less than 50°C, more preferably approximately 40°C or less (typically a rosin-based, terpene-based, hydrocarbon-based, etc. tackifying resin, e.g. Hydrogenated rosin methyl ester, etc.) may or may not be included.
- a low softening point tackifier resin may be a liquid tackifier resin that exhibits a liquid state at 30°C.
- the liquid tackifying resin can be used alone or in combination of two or more.
- the content of the liquid tackifying resin can be approximately 30% by weight or less of the entire tackifier resin T L from the viewpoint of cohesive force etc., and should be approximately 10% by weight or less (for example, 0 to 10% by weight). is suitable, and may be approximately 2% by weight or less (0.5 to 2% by weight), and may be less than 1% by weight.
- the content of the tackifier resin T L is not particularly limited, but in some embodiments, it is appropriate to set it to about 70 parts by weight or less based on 100 parts by weight of the acrylic polymer, and even if it is 60 parts by weight or less. Generally, the amount may be 50 parts by weight or less, 40 parts by weight or less, or 30 parts by weight or less. In some preferred embodiments, the content of the tackifying resin T L is less than 30 parts by weight, more preferably 25 parts by weight or less, and even more preferably 22 parts by weight or less, based on 100 parts by weight of the acrylic polymer. The amount may be 20 parts by weight or less.
- the content of the tackifier resin T L is, for example, 1 part by weight or more, preferably 5 parts by weight or more, based on 100 parts by weight of the acrylic polymer.
- the amount is preferably 8 parts by weight or more, more preferably 10 parts by weight or more, still more preferably 12 parts by weight or more, and may be 15 parts by weight or more.
- the 23°C storage modulus tends to increase as the amount of the tackifying resin T L having an appropriate softening point increases.
- the adhesive layer combines a tackifying resin T L and a tackifying resin T H having a softening point of 150° C. or higher (for example, 150° C. to 200° C.) within a range that does not impair the effects of the invention. may also be included.
- a tackifying resin T H one kind or a combination of two or more kinds of tackifier resins having a softening point of 150° C. or more among the tackifier resins exemplified above can be used.
- the tackifier resin T L preferably accounts for more than 50% by weight of the total amount of tackifier resin contained in the pressure-sensitive adhesive layer. This makes it easier for the effect of containing the tackifier resin T L to be effectively expressed. From the viewpoint of more effectively exerting the effect of using the tackifier resin T L , the ratio of the tackifier resin T L to the total amount of tackifier resin contained in the pressure-sensitive adhesive layer is preferably 60% by weight or more, more preferably 70% by weight or more, even more preferably 80% by weight or more, particularly preferably 90% by weight or more, and may be 95% by weight or more, or may be 98% by weight or more.
- the tackifier resin contained in the pressure-sensitive adhesive layer is substantially composed of only the tackifier resin T L.
- the ratio of the tackifier resin T L to the total amount of tackifier resin contained in the pressure-sensitive adhesive layer is in the range of 99 to 100% by weight.
- the tackifier resin may include a tackifier resin (eg, terpene phenol resin) having a hydroxyl value higher than 20 mgKOH/g.
- a tackifier resin eg, terpene phenol resin
- tackifying resins having a hydroxyl value of 30 mgKOH/g or more are preferred.
- a tackifier resin having a hydroxyl value of 30 mgKOH/g or more may be referred to as a "high hydroxyl value resin”.
- a crosslinking agent such as an isocyanate-based crosslinking agent.
- the tackifier resin may include a high hydroxyl value resin having a hydroxyl value of 60 mgKOH/g or more (for example, 70 mgKOH/g or more).
- the above-mentioned high hydroxyl value resin (for example, terpene phenol resin) is preferably used in combination with, for example, an acrylic polymer containing heptyl acrylate as a monomer component, and can achieve both adhesive strength and cohesive strength.
- the upper limit of the hydroxyl value of the high hydroxyl value resin is not particularly limited.
- the hydroxyl value of the high hydroxyl value resin is usually about 300 mgKOH/g or less, suitably about 200 mgKOH/g or less, preferably about 180 mgKOH/g or less, or more.
- it is about 160 mgKOH/g or less, more preferably about 140 mgKOH/g or less, it may be 120 mgKOH/g or less, it may be 100 mgKOH/g or less, it may be 80 mgKOH/g or less (for example, 65 mgKOH/g or less).
- the tackifier resin includes a high hydroxyl value resin (for example, a terpene-based tackifier resin, preferably a terpene phenol resin) with a hydroxyl value of 30 to 160 mgKOH/g.
- a high hydroxyl value resin having a hydroxyl value of 30 to 80 mgKOH/g can be preferably employed.
- a value measured by the potentiometric titration method specified in JIS K0070:1992 can be adopted.
- the specific measurement method is as shown below.
- [Method for measuring hydroxyl value] 1.
- Reagent (1) As the acetylation reagent, take about 12.5 g (about 11.8 mL) of acetic anhydride, add pyridine to make a total volume of 50 mL, and stir thoroughly. Alternatively, take about 25 g (about 23.5 mL) of acetic anhydride, add pyridine to make a total volume of 100 mL, stir thoroughly, and use.
- (2) A 0.5 mol/L potassium hydroxide ethanol solution is used as the measurement reagent.
- the high hydroxyl value resin one having a hydroxyl value of a predetermined value or more among the various tackifying resins mentioned above can be used.
- the high hydroxyl value resins can be used alone or in combination of two or more.
- a terpene phenol resin having a hydroxyl value of 30 mgKOH/g or more can be preferably employed as the high hydroxyl value resin.
- Terpene phenol resin is advantageous because the hydroxyl value can be arbitrarily controlled by adjusting the copolymerization ratio of phenol.
- the proportion of the high hydroxyl value resin for example, terpene phenol resin
- the proportion of the high hydroxyl value resin in the entire tackifying resin is preferably about 30% by weight or more, for example. Thereby, the effect of using the high hydroxyl value resin is preferably exhibited.
- the proportion of the high hydroxyl value resin in the entire tackifying resin is about 40% by weight or more, and may be about 50% by weight or more (for example, more than 50% by weight), and about 60% by weight. % or more, approximately 70% by weight or more, approximately 80% by weight or more, or approximately 90% by weight or more. Substantially all of the tackifying resin (for example, about 95 to 100% by weight, or even about 99 to 100% by weight) may be a high hydroxyl value resin.
- the softening point of the high hydroxyl value resin is not particularly limited.
- the softening point of the high hydroxyl value resin may be, for example, approximately 50°C or higher, and from the viewpoint of improving cohesive force, a high hydroxyl value resin having a softening point (softening temperature) of approximately 80°C or higher may be preferably employed.
- a terpene phenol resin having such a softening point can be preferably used.
- the softening point of the high hydroxyl value resin may be approximately 100°C or higher, or approximately 110°C or higher.
- the upper limit of the softening point of the high hydroxyl value resin is not particularly limited.
- a high hydroxyl value resin having a softening point of approximately 200° C. or lower (more preferably approximately 180° C. or lower) may be preferably used.
- the softening point of the high hydroxyl value resin may be less than 160°C, may be less than 150°C, may be less than 145°C, may be less than 140°C, may be less than 130°C, may be less than 120°C. But that's fine.
- the content of the high hydroxyl value resin in the adhesive layer is not particularly limited as long as it satisfies the desired properties (viscoelastic properties, etc.).
- the content of the high hydroxyl value resin is usually about 1 part by weight or more, and can be about 5 parts by weight or more, based on 100 parts by weight of the acrylic polymer, from the viewpoint of improving adhesive strength. It is suitable, preferably about 8 parts by weight or more, more preferably about 10 parts by weight or more, still more preferably about 12 parts by weight or more (for example, 15 parts by weight or more).
- the content of the high hydroxyl value resin in the adhesive layer is, for example, 70 parts by weight or less, and may be 60 parts by weight or less, based on 100 parts by weight of the acrylic polymer. The amount may be 50 parts by weight or less, 40 parts by weight or less, or 30 parts by weight or less. In some preferred embodiments, the content of the high hydroxyl value resin is less than 30 parts by weight, more preferably 25 parts by weight or less, still more preferably 22 parts by weight or less, even if it is 20 parts by weight or less. good.
- the tackifier resin is preferably a tackifier resin derived from plants (vegetable tackifier resin) from the viewpoint of improving the biomass carbon ratio of the adhesive layer. It can work.
- vegetable tackifying resins include the above-mentioned rosin-based tackifying resins and terpene-based tackifying resins.
- the vegetable tackifying resins can be used alone or in combination of two or more.
- the proportion of the vegetable tackifying resin in the total amount of the tackifying resin is 30% by weight or more (for example, 50% by weight or more, typically 80% by weight). above) is preferable.
- the proportion of vegetable tackifying resin in the total amount of tackifying resin is 90% by weight or more (eg, 95% by weight or more, typically 99-100% by weight).
- the technology disclosed herein can be preferably implemented in an embodiment that does not substantially contain tackifying resins other than vegetable tackifying resins.
- the content of the tackifier resin in the adhesive layer is not particularly limited as long as the desired properties (viscoelastic properties, etc.) are satisfied.
- the content of the tackifier resin is usually about 1 part by weight or more, and is preferably about 5 parts by weight or more, and is preferably about 8 parts by weight or more, more preferably 10 parts by weight or more, and even more preferably about 12 parts by weight or more (e.g., 15 parts by weight or more) relative to 100 parts by weight of the acrylic polymer from the viewpoint of improving adhesive strength.
- the content of the tackifier resin in the adhesive layer is, for example, 70 parts by weight or less, may be 60 parts by weight or less, may be 50 parts by weight or less, may be 40 parts by weight or less, or may be 30 parts by weight or less, relative to 100 parts by weight of the acrylic polymer. In some preferred embodiments, the content of the tackifier resin is less than 30 parts by weight, more preferably 25 parts by weight or less, even more preferably 22 parts by weight or less, and may be 20 parts by weight or less.
- the adhesive layer contains an acrylic oligomer.
- the adhesive force of the pressure-sensitive adhesive can be improved.
- the adhesive layer has a composition containing an acrylic oligomer and has predetermined viscoelastic properties (specifically, 23°C storage modulus and 23°C tan ⁇ ) and gel fraction. obtain.
- the effect of using an acrylic oligomer can be effectively exhibited in a composition containing a high molecular weight acrylic polymer.
- Acrylic oligomers can be used singly or in combination of two or more.
- the acrylic oligomer has a Tg of about 0°C or more and about 300°C or less, preferably about 20°C or more and about 300°C or less, and more preferably about 40°C or more and about 300°C or less.
- Tg is within the above range, adhesive strength can be suitably improved.
- the Tg of the acrylic oligomer is about 30°C or higher, more preferably about 50°C or higher (for example, about 60°C or higher), from the viewpoint of adhesive cohesiveness, and From this point of view, the temperature is preferably about 200°C or less, more preferably about 150°C or less, and even more preferably about 100°C or less (for example, about 80°C or less).
- the Tg of the acrylic oligomer refers to the Tg determined by the Fox equation based on the composition of the monomer components, similar to the Tg of the acrylic polymer described above.
- the weight average molecular weight (Mw) of the acrylic oligomer is typically about 1,000 or more and less than about 30,000, preferably about 1,500 or more and less than about 20,000, and more preferably about 2,000 or more and less than about 10,000. When Mw is within the above range, good adhesive strength is likely to be obtained. In some preferred embodiments, the Mw of the acrylic oligomer is about 2,500 or more (for example, about 3,000 or more), and from the viewpoint of adhesiveness, it is preferably about 7,000 or less, more preferably about 5,000 or less (for example, about 4,500 or less). , typically about 4000 or less).
- the Mw of the acrylic oligomer can be measured by gel permeation chromatography (GPC) and determined as a value in terms of standard polystyrene. Specifically, the measurement is performed using HPLC8020 manufactured by Tosoh Corporation with two columns of TSKgelGMH-H (20) at a flow rate of about 0.5 mL/min using tetrahydrofuran solvent.
- GPC gel permeation chromatography
- Examples of monomers constituting the acrylic oligomer include methyl (meth)acrylate, ethyl (meth)acrylate, propyl (meth)acrylate, isopropyl (meth)acrylate, butyl (meth)acrylate, isobutyl (meth)acrylate, and s-butyl.
- acrylic oligomers include alkyl (meth)acrylates in which the alkyl group has a branched structure, such as isobutyl (meth)acrylate and t-butyl (meth)acrylate; cyclohexyl (meth)acrylate, isobornyl (meth)acrylate, and dicyclopentaacrylate; Esters of (meth)acrylic acid and alicyclic alcohol such as phenyl (meth)acrylate ((meth)acrylate containing an alicyclic hydrocarbon group); aryl such as phenyl (meth)acrylate and benzyl (meth)acrylate Containing as a monomer unit an acrylic monomer having a relatively bulky structure, such as (meth)acrylate having a cyclic structure, further improves the adhesiveness of the adhesive layer.
- alkyl (meth)acrylates in which the alkyl group has a branched structure, such as isobutyl (meth)acrylate and
- UV rays when synthesizing acrylic oligomers or preparing adhesive layers, it is preferable to use ultraviolet rays that have saturated bonds because they are less likely to inhibit polymerization, and those that have alkyl groups with a branched structure are preferable.
- Alkyl (meth)acrylates or esters with alicyclic alcohols alicyclic hydrocarbon group-containing (meth)acrylates
- alicyclic hydrocarbon group-containing (meth)acrylates can be suitably used as monomers constituting the acrylic oligomer.
- the alicyclic hydrocarbon group can be a saturated or unsaturated alicyclic hydrocarbon group.
- the proportion of (meth)acrylate monomer (for example, alicyclic hydrocarbon group-containing (meth)acrylate) in the monomer components constituting the acrylic oligomer is typically more than 50% by weight, preferably 60% by weight.
- the content is more than 70% by weight, more preferably 70% by weight or more (for example, 80% by weight or more, even 90% by weight or more).
- the acrylic oligomer has a monomer composition consisting essentially of (meth)acrylate monomers.
- functional group-containing monomers can be used as constituent monomer components of the acrylic oligomer.
- suitable examples of the functional group-containing monomer include monomers having a nitrogen atom-containing ring (typically a nitrogen atom-containing heterocycle) such as N-vinyl-2-pyrrolidone and N-acryloylmorpholine; N,N-dimethylamino Amino group-containing monomers such as ethyl (meth)acrylate; amide group-containing monomers such as N,N-diethyl (meth)acrylamide; carboxy group-containing monomers such as AA and MAA; hydroxyl group-containing monomers such as 2-hydroxyethyl (meth)acrylate Monomers;
- These functional group-containing monomers can be used alone or in combination of two or more.
- carboxy group-containing monomers are preferred, and AA is particularly preferred.
- carboxy group-containing monomer is particularly preferred.
- the proportion of the functional group-containing monomer (for example, a carboxy group-containing monomer such as AA) in the monomer component can be approximately 1% by weight or more. It is appropriate, preferably 2% by weight or more, more preferably 3% by weight or more, and approximately 15% by weight or less, preferably 10% by weight or less, more preferably 7% by weight or less. be.
- the acrylic oligomer can be formed by polymerizing its constituent monomer components.
- the polymerization method and polymerization mode are not particularly limited, and various conventionally known polymerization methods (e.g., solution polymerization, emulsion polymerization, bulk polymerization, photopolymerization, radiation polymerization, etc.) can be employed in an appropriate mode.
- the types of polymerization initiators for example, azo polymerization initiators such as AIBN
- AIBN azo polymerization initiators
- the amount of the chain transfer agent such as n-dodecyl mercaptan is appropriately determined based on common technical knowledge so as to obtain a desired molecular weight, and therefore detailed explanation will be omitted here.
- suitable acrylic oligomers include dicyclopentanyl methacrylate (DCPMA), cyclohexyl methacrylate (CHMA), isobornyl methacrylate (IBXMA), isobornyl acrylate (IBXA), dicyclopentanyl
- DCPA 1-adamantyl methacrylate
- ADMA 1-adamantyl methacrylate
- ADA 1-adamantyl acrylate
- a copolymer of CHMA and isobutyl methacrylate (IBMA) a copolymer of CHMA and IBXMA, Copolymer of CHMA and acryloylmorpholine (ACMO), copolymer of CHMA and diethylacrylamide (DEAA), copolymer of CHMA and AA, copolymer of ADA and methyl methacrylate (MMA), DCPMA and IBXMA copolymers of DCPMA and MMA, and copolymers of DCPMA and DCPMA and
- the content of the acrylic oligomer is preferably, for example, 0.1 part by weight or more (for example, 1 part by weight or more) based on 100 parts by weight of the acrylic polymer. It is. From the viewpoint of better exhibiting the effects of the acrylic oligomer, the content of the acrylic oligomer is preferably about 3 parts by weight or more, more preferably about 5 parts by weight or more, and about 8 parts by weight or more. The amount may be approximately 10 parts by weight or more. Further, from the viewpoint of compatibility with the acrylic polymer, in some embodiments, the content of the acrylic oligomer is less than 50 parts by weight (for example, less than 40 parts by weight) based on 100 parts by weight of the acrylic polymer.
- the amount is preferably less than 30 parts by weight, more preferably about 25 parts by weight or less, even more preferably about 20 parts by weight or less.
- the content of the acrylic oligomer is less than 20 parts by weight, may be 15 parts by weight or less, may be 12 parts by weight or less, and may be 10 parts by weight or less, based on 100 parts by weight of the acrylic polymer.
- the amount may be less than 8 parts by weight, or less than 6 parts by weight.
- the content of the acrylic oligomer may be 5 parts by weight or less, or 1 part by weight or less (for example, less than 1 part by weight) based on 100 parts by weight of the acrylic polymer.
- the technique disclosed herein can be implemented in an embodiment in which the adhesive layer does not substantially contain an acrylic oligomer.
- the adhesive layer contains one or more of the above-mentioned tackifier resins and one or more acrylic oligomers.
- a composition containing an acrylic polymer excellent adhesiveness can be obtained by using a tackifier resin and an acrylic oligomer together.
- the effects of the technology disclosed herein can be preferably achieved in a composition containing an acrylic polymer containing heptyl acrylate as a monomer component, a tackifier resin, and an acrylic oligomer.
- the effect of using a tackifier resin and an acrylic oligomer in combination can be effectively exhibited.
- the ratio (C T /C O ) of the tackifying resin content C T [wt%] to the acrylic oligomer content C O [wt %] in the adhesive layer is not particularly limited, and is, for example, 0.1. It is appropriate to set the value to 10 or less. In some embodiments, the ratio (C T /C O ) is greater than or equal to 0.25, may be greater than or equal to 0.4, may be greater than or equal to 0.7, and may be greater than or equal to 0.8. The higher the ratio (C T /C O ) is, the more effectively the effect of adding the tackifier resin can be exhibited.
- the ratio (C T /C O ) is approximately 1 or more (for example, more than 1.0), more preferably 1.5 or more, still more preferably 2.0 or more, and 2. It may be 5 or more, 3.0 or more, or 3.5 or more. Further, from the viewpoint of obtaining the effect of adding the acrylic oligomer, in some embodiments, the above ratio (C T /C O ) is approximately 9 or less, preferably 7 or less, and may be 5 or less, It may be 3 or less. In some other embodiments, the ratio (C T /C O ) may be 2 or less, 1.5 or less, or 1.2 or less.
- the combined amount (total amount) of the tackifier resin and acrylic oligomer contained in the adhesive layer is, from the viewpoint of favorably exerting the effects of the technology disclosed herein, suitably about 1 part by weight or more per 100 parts by weight of the acrylic polymer, preferably about 10 parts by weight or more, more preferably about 16 parts by weight or more, even more preferably 20 parts by weight or more, and particularly preferably 25 parts by weight or more, and is suitably less than 120 parts by weight (e.g., about 80 parts by weight or less), preferably less than 60 parts by weight, more preferably about 50 parts by weight or less, even more preferably about 40 parts by weight or less, and particularly preferably 35 parts by weight or less, and may be 30 parts by weight or less, 28 parts by weight or less, or 26 parts by weight or less.
- the total amount (total amount) of the acrylic polymer, tackifier resin, and acrylic oligomer in the adhesive layer is appropriately set so that the effect of the technology disclosed herein is exhibited, It is not limited to a specific range.
- the total amount (total amount) of the acrylic polymer, tackifier resin, and acrylic oligomer in the entire adhesive layer is 50% by weight from the viewpoint of preferably exhibiting the effects of the technology disclosed herein.
- it is about 70% by weight or more, more preferably about 90% by weight or more, even more preferably 95% by weight or more (for example, 95% by weight or more and 100% by weight or less, or less than 100% by weight). It may be 98% by weight or more.
- the adhesive composition used to form the adhesive layer may contain a crosslinking agent as necessary.
- the type of crosslinking agent is not particularly limited, and examples include isocyanate crosslinking agents, epoxy crosslinking agents, oxazoline crosslinking agents, aziridine crosslinking agents, melamine crosslinking agents, peroxide crosslinking agents, urea crosslinking agents, and metals. Examples include alkoxide crosslinking agents, metal chelate crosslinking agents, metal salt crosslinking agents, carbodiimide crosslinking agents, hydrazine crosslinking agents, amine crosslinking agents, and silane coupling agents.
- crosslinking agent can be used alone or two or more types can be used in combination. Among these, isocyanate crosslinking agents, epoxy crosslinking agents, oxazoline crosslinking agents, aziridine crosslinking agents, and melamine crosslinking agents are preferred, and isocyanate crosslinking agents and epoxy crosslinking agents are more preferred.
- the pressure-sensitive adhesive layer can obtain an appropriate cohesive force and form a pressure-sensitive adhesive with a good balance between adhesive force and cohesive force.
- the gel fraction and 23°C storage modulus can be increased.
- the adhesive layer in the technology disclosed herein may contain the crosslinking agent in a form after a crosslinking reaction, a form before a crosslinking reaction, a partially crosslinked form, an intermediate or composite form thereof, etc. May contain.
- the crosslinking agent is typically contained in the adhesive layer exclusively in the form after crosslinking reaction.
- polyfunctional isocyanates referring to compounds having an average of two or more isocyanate groups per molecule, including those having an isocyanurate structure
- the isocyanate crosslinking agents can be used alone or in combination of two or more.
- polyfunctional isocyanates include aliphatic polyisocyanates, alicyclic polyisocyanates, aromatic polyisocyanates, and the like.
- aliphatic polyisocyanates include 1,2-ethylene diisocyanate; tetramethylene diisocyanates such as 1,2-tetramethylene diisocyanate, 1,3-tetramethylene diisocyanate, and 1,4-tetramethylene diisocyanate; 1,2-tetramethylene diisocyanate; - hexamethylene diisocyanate such as hexamethylene diisocyanate, 1,3-hexamethylene diisocyanate, 1,4-hexamethylene diisocyanate, 1,5-hexamethylene diisocyanate, 1,6-hexamethylene diisocyanate, 2,5-hexamethylene diisocyanate; Examples include 2-methyl-1,5-pentane diisocyanate, 3-methyl-1,5-pentane diisocyanate, ly
- alicyclic polyisocyanates include isophorone diisocyanate; cyclohexyl diisocyanates such as 1,2-cyclohexyl diisocyanate, 1,3-cyclohexyl diisocyanate, and 1,4-cyclohexyl diisocyanate; 1,2-cyclopentyl diisocyanate, and 1,3-cyclohexyl diisocyanate; -Cyclopentyl diisocyanates such as cyclopentyl diisocyanate; hydrogenated xylylene diisocyanate, hydrogenated tolylene diisocyanate, hydrogenated diphenylmethane diisocyanate, hydrogenated tetramethylxylene diisocyanate, 4,4'-dicyclohexylmethane diisocyanate, and the like.
- aromatic polyisocyanates include 2,4-tolylene diisocyanate, 2,6-tolylene diisocyanate, 4,4'-diphenylmethane diisocyanate, 2,4'-diphenylmethane diisocyanate, and 2,2'-diphenylmethane diisocyanate.
- polyfunctional isocyanates examples include polyfunctional isocyanates having an average of three or more isocyanate groups per molecule.
- Such trifunctional or higher functional isocyanates are polymers (typically dimers or trimers) of bifunctional or trifunctional or higher functional isocyanates, derivatives (for example, combinations of polyhydric alcohols and two or more molecules of polyfunctional isocyanates). addition reaction products), polymers, etc.
- dimers and trimers of diphenylmethane diisocyanate dimers and trimers of diphenylmethane diisocyanate, isocyanurates of hexamethylene diisocyanate (trimeric adducts of isocyanurate structures), reaction products of trimethylolpropane and tolylene diisocyanate, and products of the reaction between trimethylolpropane and hexamethylene diisocyanate.
- polyfunctional isocyanates such as reaction products with methylene diisocyanate, polymethylene polyphenylisocyanate, polyether polyisocyanate, and polyester polyisocyanate.
- the technology disclosed herein can be preferably implemented in an embodiment in which at least an isocyanate-based crosslinking agent is used as a crosslinking agent.
- the amount of the isocyanate crosslinking agent used is not particularly limited.
- the amount of the isocyanate crosslinking agent used can be, for example, about 0.1 part by weight or more based on 100 parts by weight of the acrylic polymer. From the perspective of achieving both cohesive force and adhesion, the amount of isocyanate crosslinking agent used per 100 parts by weight of the acrylic polymer should usually be approximately 0.3 parts by weight or more (for example, 0.5 parts by weight or more). is preferred.
- the amount of the isocyanate crosslinking agent used per 100 parts by weight of the acrylic polymer is about 1.0 parts by weight or more, more preferably about 1.5 parts by weight or more, and still more preferably about 2.0 parts by weight. It is more than 2.5 parts by weight, particularly preferably about 2.5 parts by weight or more, and may be about 2.8 parts by weight or more.
- the amount of the isocyanate crosslinking agent used is suitably 10 parts by weight or less, preferably 8 parts by weight or less, per 100 parts by weight of the acrylic polymer. , more preferably 6 parts by weight or less, still more preferably 5 parts by weight or less, particularly preferably 4 parts by weight or less, may be 3.5 parts by weight or less, and may be 3.2 parts by weight or less.
- epoxy crosslinking agent any compound having two or more epoxy groups in one molecule can be used without particular limitation. Epoxy crosslinking agents having 3 to 5 epoxy groups in one molecule are preferred. The epoxy crosslinking agents can be used alone or in combination of two or more.
- epoxy crosslinking agents include N,N,N',N'-tetraglycidyl-m-xylene diamine, 1,3-bis(N,N-diglycidylaminomethyl ) cyclohexane, 1,6-hexanediol diglycidyl ether, polyethylene glycol diglycidyl ether, polyglycerol polyglycidyl ether, and the like.
- epoxy crosslinking agents include Mitsubishi Gas Chemical's product names “TETRAD-C” and “TETRAD-X”, DIC's product name “Epicron CR-5L”, and Nagase ChemteX's product name Examples include the product name “Denacol EX-512” manufactured by Nissan Chemical Industries, Ltd. and the product name "TEPIC-G” manufactured by Nissan Chemical Industries, Ltd.
- the amount of the epoxy crosslinking agent used is not particularly limited.
- the amount of the epoxy crosslinking agent used may be, for example, more than 0 parts by weight and no more than about 1 part by weight (typically about 0.001 to 1 part by weight) per 100 parts by weight of the acrylic polymer. can. From the viewpoint of suitably exhibiting the effect of improving cohesive force, the amount of the epoxy crosslinking agent used is usually approximately 0.002 parts by weight or more per 100 parts by weight of the acrylic polymer, preferably The amount may be approximately 0.005 part by weight or more, for example, approximately 0.01 part by weight or more, or approximately 0.02 part by weight or more.
- the amount of the epoxy crosslinking agent used can be approximately 0.7 parts by weight or less per 100 parts by weight of the acrylic polymer, It is suitably about 0.5 parts by weight or less, preferably about 0.2 parts by weight or less, more preferably about 0.1 parts by weight or less (for example, less than 0.1 parts by weight), and about 0.07 parts by weight or less.
- the amount may be 0.04 parts by weight or less, or may be 0.03 parts by weight or less.
- an isocyanate crosslinking agent and at least one crosslinking agent having a different type of crosslinkable functional group from the isocyanate crosslinking agent are used in combination.
- the technology disclosed herein uses a crosslinking agent other than an isocyanate crosslinking agent (that is, a crosslinking agent with a different type of crosslinkable reactive group from an isocyanate crosslinking agent, hereinafter also referred to as a "non-isocyanate crosslinking agent") and an isocyanate. It can be preferably carried out in an embodiment in which the method is used in combination with a crosslinking agent.
- non-isocyanate crosslinking agent that can be used in combination with the isocyanate crosslinking agent is not particularly limited, and can be appropriately selected from the above-mentioned crosslinking agents.
- the non-isocyanate crosslinking agents can be used alone or in combination of two or more.
- an epoxy crosslinker can be employed as the non-isocyanate crosslinker.
- better adhesive properties can be achieved by using an isocyanate crosslinking agent and an epoxy crosslinking agent in combination.
- the relationship between the content of the isocyanate crosslinking agent and the content of the non-isocyanate crosslinking agent is not particularly limited, and may be determined appropriately within a range that satisfies predetermined viscoelastic properties and gel fraction. Set.
- the content of the isocyanate crosslinking agent is, for example, greater than 1 time, may be approximately 5 times or more, or approximately 10 times the content of the non-isocyanate crosslinking agent (preferably an epoxy crosslinking agent). or more, preferably about 50 times or more, more preferably about 80 times or more, still more preferably about 100 times or more (for example, more than 100 times), particularly preferably about 120 times or more (for example, about 140 times). above).
- a non-isocyanate crosslinking agent preferably an epoxy crosslinking agent
- the content of the isocyanate crosslinking agent relative to the content of the crosslinking agent (crosslinking agent) is, for example, approximately 1000 times or less, suitably approximately 500 times or less, preferably approximately 300 times or less, and more preferably approximately 200 times or less. , more preferably about 180 times or less (for example, about 160 times or less).
- the content of crosslinking agent (total amount of crosslinking agent) in the adhesive composition disclosed herein is not particularly limited. From the viewpoint of cohesion, the content of the crosslinking agent is usually about 0.001 parts by weight or more, and preferably about 0.01 parts by weight or more, based on 100 parts by weight of the acrylic polymer. Preferably it is about 0.1 part by weight or more, more preferably about 1 part by weight or more, still more preferably about 2 parts by weight or more, particularly preferably about 2.5 parts by weight or more.
- the content of the crosslinking agent in the adhesive composition is usually about 20 parts by weight or less, preferably about 15 parts by weight or less, and about 10 parts by weight, based on 100 parts by weight of the acrylic polymer. The following is preferable. In some preferred embodiments, the content of the crosslinking agent per 100 parts by weight of the acrylic polymer is 5.0 parts by weight or less, may be 4.0 parts by weight or less, or may be 3.5 parts by weight or less.
- the adhesive composition may optionally contain a leveling agent, a crosslinking aid, a plasticizer, a softener, a filler, an antistatic agent, an antiaging agent, an ultraviolet absorber, an antioxidant, Various additives common in the adhesive field, such as rust preventives and light stabilizers, may be included. Regarding such various additives, conventionally known ones can be used in a conventional manner, and since they do not particularly characterize the present invention, detailed explanations will be omitted.
- the adhesive layer (layer consisting of an adhesive) disclosed herein is formed from a water-based adhesive composition, a solvent-based adhesive composition, a hot-melt adhesive composition, or an active energy ray-curable adhesive composition. It may be an adhesive layer.
- the aqueous adhesive composition refers to an adhesive composition containing an adhesive (adhesive layer forming component) in a water-based solvent (aqueous solvent), and is typically a water-based adhesive composition. This includes what is called a type adhesive composition (a composition in which at least a portion of an adhesive is dispersed in water).
- a solvent-based adhesive composition refers to an adhesive composition containing an adhesive in an organic solvent.
- organic solvent contained in the solvent-based adhesive composition one or more of the organic solvents (toluene, ethyl acetate, etc.) that can be used in the above-mentioned solution polymerization can be used without particular limitation.
- the technology disclosed herein can be preferably implemented in an embodiment including an adhesive layer formed from a solvent-based adhesive composition from the viewpoint of adhesive properties and the like.
- the adhesive layer disclosed herein can be formed by a conventionally known method.
- a method can be adopted in which a pressure-sensitive adhesive layer is formed by applying a pressure-sensitive adhesive composition to a surface having peelability (peelability surface) or a non-peelability surface and drying it.
- a method direct method of forming an adhesive layer by directly applying (typically coating) an adhesive composition to the base material and drying is adopted.
- a method transfer method in which an adhesive composition is applied to a surface that has releasability (release surface) and dried to form an adhesive layer on the surface, and the adhesive layer is transferred to a base material.
- the transfer method is preferred.
- the release surface the surface of a release liner, the back surface of a release-treated base material, etc. can be used.
- the adhesive composition can be applied using a conventionally known coater such as a gravure roll coater, die coater, or bar coater. Alternatively, the adhesive composition may be applied by impregnation, curtain coating, or the like. From the viewpoint of promoting crosslinking reaction, improving production efficiency, etc., it is preferable to dry the adhesive composition under heating.
- the drying temperature can be, for example, about 40 to 150°C, and usually preferably about 60 to 130°C.
- aging may be performed for the purpose of adjusting component migration within the pressure-sensitive adhesive layer, progressing the crosslinking reaction, alleviating distortion that may exist within the pressure-sensitive adhesive layer, and the like.
- the adhesive layer may have a single layer structure or a multilayer structure of two or more layers. From the viewpoint of productivity etc., it is preferable that the adhesive layer has a single layer structure.
- the thickness of the adhesive layer is not particularly limited, and a configuration having an adhesive layer having an appropriate thickness in the range of, for example, 0.1 to 500 ⁇ m may be adopted depending on the use and purpose of use.
- the thickness of the adhesive layer is usually approximately 100 ⁇ m or less, preferably approximately 70 ⁇ m or less, more preferably approximately 60 ⁇ m or less, More preferably, it is about 50 ⁇ m or less, and may be about 40 ⁇ m or less.
- the thickness of the adhesive layer can be approximately 35 ⁇ m or less, for example, approximately 30 ⁇ m or less, or 20 ⁇ m or less (for example, 15 ⁇ m or less).
- the lower limit of the thickness of the adhesive layer is suitably about 0.5 ⁇ m or more, from the viewpoint of adhesion to the adherend, it may be about 1 ⁇ m or more, and it may be about 3 ⁇ m or more. It is advantageous to do so.
- the thickness of the adhesive layer is greater than 5 ⁇ m, more preferably about 10 ⁇ m or more, even more preferably about 12 ⁇ m or more (e.g., greater than 12 ⁇ m), even more preferably about 15 ⁇ m or more, e.g. It may be 18 ⁇ m or more.
- the thickness of the adhesive layer By making the thickness of the adhesive layer larger than 5 ⁇ m, fine uneven deformation can be easily eliminated due to the relaxation effect of the adhesive layer. Furthermore, as the thickness of the adhesive layer increases, the adhesive strength tends to improve as well. In more preferred embodiments, the thickness of the adhesive layer may be more than 20 ⁇ m, 24 ⁇ m or more, 27 ⁇ m or more, about 30 ⁇ m or more, or about 32 ⁇ m or more. In addition, in a double-sided adhesive sheet with a base material that has a first adhesive layer and a second adhesive layer on each side of the base material, the first adhesive layer and the second adhesive layer have the same thickness. They may have different thicknesses.
- the adhesive layer disclosed herein has a gel fraction (by weight) of 25% or more. Since the adhesive layer having the above-mentioned gel fraction has appropriate hardness, it is difficult to cause visible uneven deformation.
- the gel fraction may be 35% or more, or 40% or more. In some preferred embodiments, the gel fraction is more than 40%, more preferably 45% or more, even more preferably 50% or more, may be 55% or more, or even 60% or more. Often, it may be 65% or more, or 70% or more. A pressure-sensitive adhesive layer with a high gel fraction tends to provide good processability.
- the upper limit of the gel fraction of the adhesive layer is usually suitably less than 90% from the viewpoint of adhesive strength, etc., and may be less than 85%, may be less than 80%, and may be less than 75%. It may be less than In some preferred embodiments, the gel fraction of the adhesive layer is less than 70%, more preferably less than 65%, even more preferably less than 60%, and may be less than 55%, less than 50%. But that's fine. By limiting the gel fraction of the adhesive layer to a predetermined value or less, the adhesiveness to the adherend tends to improve.
- the gel fraction of the adhesive layer is measured by the following method. That is, approximately 0.1 g of an adhesive sample (weight Wg 1 ) was wrapped in a purse-like shape with a porous polytetrafluoroethylene membrane (weight Wg 2 ) with an average pore diameter of 0.2 ⁇ m, and the opening was wrapped with an octopus thread (weight Wg 3 ). tie up
- the above-mentioned porous polytetrafluoroethylene (PTFE) membrane is available from Nitto Denko under the trade name "Nitoflon (registered trademark) NTF1122" (average pore diameter 0.2 ⁇ m, porosity 75%, thickness 85 ⁇ m) or its equivalent. use the product.
- the pressure-sensitive adhesive layer contains a biomass-derived material, and the biomass carbon ratio thereof may be a predetermined value or more.
- the biomass carbon ratio of the pressure-sensitive adhesive layer is, for example, 1% or more, and may be 10% or more, preferably 30% or more, and more preferably 50% or more.
- a high biomass carbon ratio of the pressure-sensitive adhesive means that the amount of fossil resource-based materials, such as petroleum, used is small. In this respect, the higher the biomass carbon ratio of the pressure-sensitive adhesive, the more preferable it is.
- the biomass carbon ratio of the pressure-sensitive adhesive layer may be 55% or more, 60% or more, 70% or more, 75% or more, 80% or more, or more than 80%.
- the upper limit of the biomass carbon ratio is 100% by definition, and may be 99% or less, and from the viewpoint of material availability, it may be 95% or less, or 90% or less. From the viewpoint of easily exerting good adhesive performance, in some embodiments, the biomass carbon ratio of the pressure-sensitive adhesive layer may be, for example, 90% or less, 85% or less, or 80% or less.
- the base material supporting the adhesive layer may be a resin film, paper, cloth, rubber sheet, or foamed material.
- a body sheet, metal foil, a composite of these, etc. can be used.
- paper include Japanese paper, kraft paper, glassine paper, high quality paper, synthetic paper, top coated paper, and the like.
- Examples of the fabric include woven fabrics and nonwoven fabrics made of various fibrous substances alone or in blends.
- Examples of the above-mentioned fibrous materials include cotton, staple fiber, Manila hemp, pulp, rayon, acetate fiber, polyester fiber, polyvinyl alcohol fiber, polyamide fiber, and polyolefin fiber.
- Examples of the rubber sheet include natural rubber sheet, butyl rubber sheet, and the like.
- Examples of foam sheets include foamed polyolefin sheets, foamed polyurethane sheets, foamed polychloroprene rubber sheets, and the like.
- Examples of metal foil include aluminum foil, copper foil, and the like. Note that the base material is also referred to as a base material layer in the adhesive sheet.
- the base material may be formed from a biomass-derived material or a non-biomass-derived material. From the viewpoint of producing a pressure-sensitive adhesive sheet in consideration of reducing dependence on fossil resource-based materials, biomass-derived base materials (typically resin films) are preferably used.
- the base material may be formed using a recyclable material or a recycled material (also referred to as recycled material).
- a resin film is preferably used. Resin films (for example, polyester films such as PET films) can be recycled, so whether or not they are made from plant-based materials, reusing the used resin film allows for sustainable reproduction. It is possible to reduce the environmental burden.
- a recyclable resin film or a recycled resin film is also referred to as a recycled film.
- the recycled material (for example, recycled film) may be formed from a biomass-derived material or a non-biomass-derived material.
- the base material constituting the base material-attached pressure-sensitive adhesive sheet one containing a resin film as a base film can be preferably used.
- the base film is typically an independently shape-maintainable (independent) member.
- the base material in the technology disclosed herein may be substantially composed of such a base film.
- the base material may include an auxiliary layer in addition to the base film. Examples of the auxiliary layer include a colored layer, a reflective layer, an undercoat layer, an antistatic layer, etc. provided on the surface of the base film.
- the resin film is a film whose main component is a resin material (for example, a component contained in the resin film in an amount exceeding 50% by weight).
- resin films include polyolefin resin films such as polyethylene (PE), polypropylene (PP), and ethylene-propylene copolymers; polyethylene terephthalate (PET), polybutylene terephthalate (PBT), polyethylene naphthalate (PEN), etc.
- PET polyethylene terephthalate
- PBT polybutylene terephthalate
- PEN polyethylene naphthalate
- polyester resin film vinyl chloride resin film; vinyl acetate resin film; polyimide resin film; polyamide resin film; fluororesin film; cellophane; and the like.
- the resin film may be a rubber film such as a natural rubber film or a butyl rubber film. Among these, polyester films are preferred from the viewpoint of handling and processability, and among these, PET films are particularly preferred.
- resin film is typically a non-porous sheet, and is a concept that is distinguished from so-called non-woven fabrics and woven fabrics (in other words, a concept excluding non-woven fabrics and woven fabrics).
- the resin film may be an unstretched film, a uniaxially stretched film, or a biaxially stretched film.
- such resin films may be non-foamed.
- non-foamed resin film refers to a resin film that has not been intentionally processed to form a foam.
- the non-foamed resin film may be a resin film with an expansion ratio of less than 1.1 times (for example, less than 1.05 times, typically less than 1.01 times).
- the base material may be transparent, or may have light-shielding or light-attenuating properties.
- the substrate eg, resin film
- the light transmittance (light-shielding property) of the base material can be adjusted. Adjusting the light transmittance (for example, vertical light transmittance) of the base material can be useful for adjusting the light transmittance of the base material and further the light transmittance of the adhesive sheet containing the base material.
- colorant conventionally known pigments and dyes can be used, as well as colorants that can be included in the adhesive layer.
- the colorant is not particularly limited, and may be, for example, black, gray, white, red, blue, yellow, green, yellow-green, orange, purple, gold, silver, pearl color, or the like.
- a black coloring agent can be preferably used as the coloring agent for the substrate, since light blocking properties (for example, vertical light transmittance) can be efficiently adjusted with a small amount of the coloring agent.
- Specific black colorants include those exemplified as colorants that can be included in the adhesive layer.
- pigments eg, particulate black colorants such as carbon black
- an average particle size of 10 nm to 500 nm, more preferably 10 nm to 120 nm can be used.
- the amount of colorant used in the base material is not particularly limited, and can be adjusted as appropriate so as to impart desired optical properties.
- the amount of coloring agent used is suitably about 0.1 to 30% by weight of the base material, for example 0.1 to 25% by weight (typically 0.1 to 20% by weight). can do.
- the base material may contain fillers (inorganic fillers, organic fillers, etc.), dispersants (surfactants, etc.), anti-aging agents, antioxidants, ultraviolet absorbers, Various additives such as antistatic agents, lubricants, and plasticizers may be blended.
- the blending ratio of various additives is about less than 30% by weight (for example, less than 20% by weight, typically less than 10% by weight).
- the base material may have a single layer structure, or may have a multilayer structure of two layers, three layers, or more. From the viewpoint of shape stability, the base material preferably has a single-layer structure. In the case of a multilayer structure, at least one layer (preferably all layers) is preferably a layer having a continuous structure of the above resin (for example, polyester resin).
- the method for manufacturing the base material is not particularly limited, and any conventionally known method may be appropriately adopted. For example, conventionally known general film forming methods such as extrusion molding, inflation molding, T-die casting molding, and calender roll molding can be appropriately employed.
- the base material may be colored with a colored layer disposed on the surface of the base film (preferably a resin film).
- the base film may or may not contain a colorant.
- the colored layer may be arranged on either surface of the base film, or may be arranged on both surfaces. In a configuration in which colored layers are arranged on both surfaces of the base film, the configurations of the colored layers may be the same or different.
- Such a colored layer can typically be formed by applying a colored layer forming composition containing a colorant and a binder to a base film.
- a colorant conventionally known pigments and dyes can be used, as well as colorants that can be included in the adhesive layer or resin film.
- the binder materials known in the paint or printing fields can be used without particular limitation. Examples include polyurethane, phenol resin, epoxy resin, urea melamine resin, polymethyl methacrylate, and the like.
- the composition for forming a colored layer may be, for example, a solvent type, an ultraviolet curable type, a thermosetting type, or the like.
- the colored layer can be formed by any means conventionally used for forming colored layers without particular limitation. For example, a method of forming a colored layer (printed layer) by printing such as gravure printing, flexographic printing, or offset printing can be preferably employed.
- the colored layer may have a single layer structure consisting of one layer as a whole, or may have a multilayer structure including two, three or more sub-colored layers.
- a colored layer having a multilayer structure including two or more sub-colored layers can be formed, for example, by repeatedly applying (for example, printing) a colored layer-forming composition.
- the color and amount of the colorant contained in each sub-colored layer may be the same or different.
- the thickness of the entire colored layer is suitably about 1 ⁇ m to 10 ⁇ m, preferably about 1 ⁇ m to 7 ⁇ m, and can be, for example, about 1 ⁇ m to 5 ⁇ m.
- the thickness of each sub-colored layer is preferably about 1 ⁇ m to 2 ⁇ m.
- the surface of the base material may be subjected to conventionally known surface treatments such as corona discharge treatment, plasma treatment, ultraviolet irradiation treatment, acid treatment, alkali treatment, and application of an undercoat.
- Such surface treatment may be a treatment for improving the adhesion between the base material and the adhesive layer, in other words, the ability of the adhesive layer to anchor to the base material.
- the back surface of the base material may be subjected to a peeling treatment as necessary.
- the peeling treatment is performed by applying a general silicone-based, long-chain alkyl-based, or fluorine-based peeling agent to a thin film, typically about 0.01 ⁇ m to 1 ⁇ m (for example, 0.01 ⁇ m to 0.1 ⁇ m). It can be a process to add. By performing such a peeling treatment, effects such as facilitating the unwinding of a roll-shaped adhesive sheet can be obtained.
- the thickness of the base material is not particularly limited. From the viewpoint of preventing the pressure-sensitive adhesive sheet from becoming too thick, the thickness of the base material can be, for example, approximately 200 ⁇ m or less, preferably approximately 150 ⁇ m or less, and more preferably approximately 100 ⁇ m or less.
- the thickness of the base material may be approximately 70 ⁇ m or less, approximately 50 ⁇ m or less, or approximately 30 ⁇ m or less (for example, approximately 25 ⁇ m or less) depending on the purpose and manner of use of the adhesive sheet. In some embodiments, the thickness of the substrate can be about 20 ⁇ m or less, about 15 ⁇ m or less, about 10 ⁇ m or less (eg, about 5 ⁇ m or less).
- the thickness of the adhesive layer can be increased even if the total thickness of the adhesive sheet is the same, which improves adhesion to the adherend and base material. It can be advantageous from
- the thickness of the base material is usually about 0.5 ⁇ m or more (for example, 1 ⁇ m or more), preferably about 2 ⁇ m or more, for example about 6 ⁇ m or more, from the viewpoint of handleability and processability of the pressure-sensitive adhesive sheet.
- the total thickness of the adhesive sheet disclosed herein (which includes an adhesive layer and may further include a base layer, but does not include a release liner) is not particularly limited.
- the total thickness of the adhesive sheet is, for example, approximately 1 mm or less, may be approximately 500 ⁇ m or less, and may be approximately 300 ⁇ m or less, and from the viewpoint of thinning, approximately 200 ⁇ m or less is appropriate, and approximately 150 ⁇ m or less. (For example, approximately 100 ⁇ m or less).
- the thickness of the pressure-sensitive adhesive sheet can be about 50 ⁇ m or less, for example, about 35 ⁇ m or less.
- the lower limit of the thickness of the adhesive sheet is, for example, 0.1 ⁇ m or more (for example, 0.5 ⁇ m or more), suitably about 3 ⁇ m or more, preferably about 10 ⁇ m or more, more preferably about 15 ⁇ m or more, More preferably, it is approximately 20 ⁇ m or more, may be approximately 30 ⁇ m or more, and may be approximately 50 ⁇ m or more.
- a pressure-sensitive adhesive sheet having a thickness of a predetermined value or more tends to have good adhesion to an adherend and also tends to have excellent handling properties.
- the thickness of the adhesive layer is the total thickness of the adhesive sheet.
- a release liner can be used during formation of the adhesive layer, production of the adhesive sheet, storage of the adhesive sheet before use, distribution, shape processing, etc.
- the release liner is not particularly limited, and for example, a release liner having a release treatment layer on the surface of a liner base material such as a resin film or paper, a release liner made of a fluorine-based polymer (polytetrafluoroethylene, etc.), etc. may be used. be able to.
- the release treatment layer may be formed by surface-treating the liner base material with a release agent such as a silicone-based, long-chain alkyl-based, fluorine-based, or molybdenum sulfide release agent.
- a release agent such as a silicone-based, long-chain alkyl-based, fluorine-based, or molybdenum sulfide release agent.
- the liner base material like the base material of the above-mentioned adhesive sheet, one formed using a biomass-derived material or a recycled material (recycled film, etc.) can be preferably used.
- the release liner disclosed herein may include a release liner base.
- a material having a release treatment layer on the material can be preferably used.
- the release treatment layer may be formed by surface treating a release liner base material with a release treatment agent.
- the release agent may be a known release agent such as a silicone release agent, a long chain alkyl release agent, a fluorine release agent, or molybdenum (IV) sulfide.
- a release liner having a release layer formed of a silicone release agent may be preferably employed.
- the thickness and formation method of the release treatment layer are not particularly limited, and can be set so that appropriate release properties are exhibited on the adhesive side surface of the release liner.
- a plastic film is typically a non-porous sheet, and is a concept that is distinguished from, for example, nonwoven fabric (that is, it does not include nonwoven fabric).
- a resin film having a non-porous structure and typically substantially free of air bubbles (voidless) may preferably be used.
- the resin film may have a single layer structure or a multilayer structure of two or more layers (for example, a three layer structure).
- polyester resins such as polyethylene terephthalate (PET), polybutylene terephthalate (PBT), and polyethylene naphthalate (PEN), polyethylene (PE), polypropylene (PP), and ethylene-propylene copolymer.
- Polyolefin resins such as ethylene-butene copolymers, cellulose resins such as triacetylcellulose, acetate resins, polysulfone resins, polyethersulfone resins, polycarbonate resins, polyamide resins, polyimide resins, norbornene resins
- Cyclic polyolefin resins such as resins, (meth)acrylic resins, polyvinyl chloride resins, polyvinylidene chloride resins, polystyrene resins, polyvinyl alcohol resins, ethylene-vinyl acetate copolymer resins, ethylene-vinyl alcohol copolymers
- Examples include coalescent resin, polyarylate resin, polyphenylene sulfide resin, and the like.
- a release liner base material formed from any one type of these resins or a mixture of two or more types can be used. Among them, a preferred release liner base material is a polyester resin film (for example, PET film) formed from
- the plastic film used as the above-mentioned release liner base material may be any of an unstretched film, a uniaxially stretched film, and a biaxially stretched film. Further, the plastic film may have a single layer structure or a multilayer structure including two or more sublayers.
- the above plastic film contains antioxidants, anti-aging agents, heat stabilizers, light stabilizers, ultraviolet absorbers, colorants such as pigments and dyes, lubricants, fillers, antistatic agents, slip agents, anti-blocking agents, Known additives that can be used in release liner base materials, such as nucleating agents, may be blended. In a multilayer plastic film, each additive may be blended in all sublayers, or may be blended only in some sublayers.
- the thickness of the release liner is not particularly limited, and may be, for example, about 10 ⁇ m to 500 ⁇ m. From the viewpoint of strength and dimensional stability of the release liner, the thickness of the release liner is suitably 20 ⁇ m or more, preferably 25 ⁇ m or more, may be 30 ⁇ m or more, and may be 35 ⁇ m or more.
- the smoothness of the adhesive surface is easily maintained. For example, uneven deformation of the adhesive layer is less likely to occur due to external force from the back surface of the release liner or foreign matter present on the back surface of the release liner.
- the thickness of the release liner is suitably 300 ⁇ m or less, preferably 200 ⁇ m or less, and may be 150 ⁇ m or less. It may be 100 ⁇ m or less.
- the thickness of the release liner may be 75 ⁇ m or less, 60 ⁇ m or less, 50 ⁇ m or less, 40 ⁇ m or less, or 30 ⁇ m or less. According to the technology disclosed herein, even if minute unevenness deformation such as dents occurs in the adhesive layer due to external force or foreign matter from the back of the release liner, the adhesive layer has excellent ability to alleviate unevenness deformation. , the above-mentioned fine unevenness deformation can be eliminated or softened, and good appearance quality can be imparted.
- the thicknesses of the first release liner and the second release liner are the same. may be different. From the viewpoint of release workability, etc., it is preferable that the first release liner and the second release liner have different thicknesses, and the thickness of the thicker release liner is approximately 1 ounce of the thickness of the thinner release liner. It is preferable to have a thickness of .1 times or more, for example, about 1.25 times or more.
- a roll body (adhesive sheet roll with release liner) including the adhesive sheet with release liner disclosed herein in a wound form is provided.
- One of the effects of the technology disclosed herein is unevenness deformation relaxation, which is caused by minute foreign matter in the adhesive layer that is mixed into the back surface of the release liner when the adhesive sheet with a release liner is wound onto a roll. Effective against uneven deformation.
- the technology disclosed herein is suitable for adhesive sheets that are stored in a roll form before use.
- the roll body as described above typically includes a core and an adhesive sheet with a release liner wound around the core.
- the shape of the core is not particularly limited, and may be, for example, a solid cylinder, a hollow cylinder (ie, cylindrical shape), a hollow or solid polygonal cylinder, or the like. From the viewpoint of improving the handling properties of the roll body, a hollow cylindrical or hollow polygonal column core can be preferably employed. Particularly preferred is a cylindrical core.
- the light transmittance of the adhesive sheet varies depending on the purpose of use, the purpose of coloring, etc., and is not limited to a specific range.
- the light transmittance at a wavelength of 550 nm (550 nm light transmittance, also referred to as visible light transmittance) of the adhesive sheet is less than 80%, may be less than 70%, and may be less than 60%. , may be less than 50%, or may be less than 40%.
- a pressure-sensitive adhesive sheet whose visible light transmittance is limited to a predetermined value or less by coloring the pressure-sensitive adhesive layer is suitable for hiding an adherend, and can also be used to impart design properties.
- the 550 nm light transmittance of the adhesive sheet is 30% or less, may be 20% or less, may be 15% or less, may be 10% or less, may be 8% or less, and may be 6% or less. It may be less than %. The lower the visible light transmittance, the more excellent hiding power can be exhibited. When higher hiding power is required, the 550 nm light transmittance may be less than 5%, less than 4%, less than 3%, less than 2%, less than 1%, or 0. It may be less than .5%.
- the lower limit of the 550 nm light transmittance is not particularly limited, and may be substantially 0%, that is, below the detection limit, 0.1% or more, 1% or more, or 3% or more. Often, it may be 5% or more. In some embodiments, the 550 nm light transmittance may be 10% or more, more than 20%, or more than 30%.
- a pressure-sensitive adhesive sheet having appropriate light transmittance is preferable from the viewpoint of maintaining adhesive properties and productivity.
- the light transmittance of the adhesive sheet at a wavelength of 1380 nm (1380 nm light transmittance, also referred to as infrared transmittance) is less than 90%, may be less than 80%, and may be less than 70%. It may be less than 60%, it may be less than 50%, it may be less than 40%. In some preferred embodiments, the 1380 nm light transmittance of the adhesive sheet is 30% or less, may be 20% or less, may be 15% or less, may be 10% or less, may be 5% or less, It may be less than %. Further, for example, when used near an infrared sensor, by blocking infrared rays, it is possible to prevent a decrease in the operational accuracy of the sensor.
- the pressure-sensitive adhesive sheet with limited infrared transmittance it is possible to block light in a wide wavelength range including infrared rays, and it is easy to obtain excellent light blocking properties.
- the lower limit of the 1380 nm light transmittance is not particularly limited, and may be substantially 0%, that is, below the detection limit, 0.1% or more, 1% or more, or 3% or more. Often, it may be 5% or more. In some embodiments, the 1380 nm light transmittance may be 10% or more, 30% or more, or 50% or more.
- the relative relationship between visible light transmittance and infrared transmittance of the adhesive sheet is not particularly limited.
- the ratio of the infrared transmittance T IR [%] to the visible light transmittance T VL [%] (T IR /T VL ) of the adhesive sheet is, for example, within the range of 0.1 to 10. , may be 5 or less, may be 3 or less, may be 0.5 or more, may be 1 or more (for example, more than 1), or may be 2 or more.
- the adhesive sheet preferably has a 180 degree peel strength against a stainless steel plate (adhesive strength against SUS) of approximately 1 N/25 mm or more, and approximately 5 N/25 mm or more. It is.
- the adhesive force to SUS is about 10 N/25 mm or more, may be about 12 N/25 mm or more, more preferably about 15 N/25 mm or more, still more preferably about 18 N/25 mm or more. , particularly preferably 20 N/25 mm or more (for example, 22 N/25 mm or more).
- the pressure-sensitive adhesive sheet exhibiting the above-mentioned adhesive strength against SUS exhibits good adhesive strength to adherends and is preferably used for joining and fixing members.
- the upper limit of the adhesive force to SUS is not particularly limited, but from the viewpoint of coexistence with other adhesive properties, it is usually about 50 N/25 mm or less, and in some embodiments, it may be about 30 N/25 mm or less. good.
- the adhesive strength to SUS is measured using an SUS plate as an adherend under the conditions of a tensile speed of 300 mm/min and a peel angle of 180 degrees in a measurement environment of 23° C. and 50% RH. More specifically, it is measured by the following method.
- Adhesive strength to SUS Under a measurement environment of 23°C and 50% RH, one adhesive side of an adhesive sheet (double-sided adhesive sheet) was lined with a PET film with a thickness of 50 ⁇ m, and cut into a size of 25 mm in width and 100 mm in length. Prepare a measurement sample. In an environment of 23° C.
- the other adhesive surface of the measurement sample is pressed onto the surface of a stainless steel plate (SUS304BA plate) that has been cleaned with ethyl acetate by making one reciprocation with a 2 kg roller.
- the peel strength (relative to SUS Adhesive force) [N/25mm] is measured.
- the universal tensile compression tester used is Minebea's "Tensile Compression Tester, TG-1kN" or its equivalent. Note that when performing the above peel strength measurement on a single-sided adhesive sheet, backing with a PET film is not necessary.
- the base material thickness is thin (for example, when the base material thickness is 25 ⁇ m or less), it may be lined with a PET film.
- the pressure-sensitive adhesive sheet contains a biomass-derived material, and the biomass carbon ratio thereof may be a predetermined value or more.
- the biomass carbon ratio of the pressure-sensitive adhesive sheet is, for example, 1% or more, and may be 10% or more, preferably 30% or more, and more preferably 50% or more.
- a high biomass carbon ratio of the pressure-sensitive adhesive sheet means that the amount of fossil resource-based materials, such as petroleum, used is small. In this respect, the higher the biomass carbon ratio of the pressure-sensitive adhesive sheet, the more preferable it is.
- the biomass carbon ratio of the pressure-sensitive adhesive sheet may be 55% or more, 60% or more, 70% or more, 75% or more, 80% or more, or more than 80%.
- the upper limit of the biomass carbon ratio is 100% by definition, and may be 99% or less, and from the viewpoint of material availability, it may be 95% or less, or 90% or less. From the viewpoint of making it easier to exhibit good adhesive performance, in some embodiments, the biomass carbon ratio of the pressure-sensitive adhesive sheet may be, for example, 90% or less, 85% or less, or 80% or less.
- the adhesive sheet disclosed herein has a colored adhesive layer, highly suppresses fine unevenness deformation, and has an adhesive surface with excellent appearance quality, so it can be applied to the surface of an adherend.
- Applications where the attached adhesive sheet is visible such as applications where the adhesive sheet is required to have concealing properties, applications where a colored adhesive layer is used to add design or color, and other specified applications. It is suitable for various uses such as those requiring optical properties (light transmittance, etc.).
- some electronic devices such as portable electronic devices require the use of adhesive sheets to conceal components and adjust the appearance.
- the adhesive sheet disclosed herein is suitable for such electronic devices.
- Non-limiting examples of the above-mentioned portable electronic devices include mobile phones, smartphones, tablet computers, notebook computers, and various wearable devices (e.g., wrist-wear type that is worn on the wrist like a wristwatch, and Modular type that is attached to a part of the body, eyewear type that includes glasses type (monocular type and binocular type, including head-mounted type), clothing type that is attached to shirts, socks, hats, etc. in the form of accessories, and earphones. digital cameras, digital video cameras, audio equipment (portable music players, IC recorders, etc.), calculators (calculators, etc.), portable game devices, electronic dictionaries, electronic notebooks, electronic books, and in-vehicle devices.
- wearable devices e.g., wrist-wear type that is worn on the wrist like a wristwatch, and Modular type that is attached to a part of the body
- eyewear type that includes glasses type (monocular type and binocular type, including head-mounted type)
- clothing type that is attached
- portable does not mean that it is sufficient to simply be able to carry it; it also means that it has a level of portability that allows an individual (standard adult) to carry it relatively easily. shall mean.
- the electronic devices include personal computers (desktop type, notebook type, tablet type, etc.), televisions, and the like. These may include a built-in display device such as a liquid crystal or organic EL.
- the adhesive sheet can be used for the purpose of fixing a pressure-sensitive sensor and other members in, for example, a portable electronic device including a pressure-sensitive sensor among the above-mentioned portable electronic devices.
- the adhesive sheet includes a device for indicating a position on the screen (typically a pen-shaped or mouse-shaped device) and a device for detecting the position, and a plate corresponding to the screen ( Used to fix a pressure-sensitive sensor and other components in an electronic device (typically a portable electronic device) that has a function that allows specifying an absolute position on a touch panel (typically a touch panel). It can be done.
- the adhesive sheet is suitable for use in being placed on the back surface of a display screen (display section) such as a touch panel display in a portable electronic device.
- a display screen such as a touch panel display in a portable electronic device.
- the adhesive sheet is suitable for portable electronic devices with built-in optical sensors.
- the various devices mentioned above, such as the portable electronic devices use light rays such as infrared, visible, and ultraviolet light for the purpose of operating the device, sensing nearby objects, detecting surrounding brightness (environmental light), and data communication.
- It may include a light sensor.
- examples of the optical sensor include an acceleration sensor, a proximity sensor, a brightness sensor (environmental light sensor), and the like.
- Such an optical sensor has a light-receiving element for light such as ultraviolet light, visible light, and infrared light, and may also have a light-emitting element for specific light such as infrared light.
- the optical sensor may include a light emitting element and/or a light receiving element for emitting light in a specific wavelength range among wavelength ranges including ultraviolet rays, visible light, and infrared rays.
- Adhesive sheets according to some embodiments are applied to such devices to limit the entry of light that may be refracted or scattered within the adhesive layer, thereby controlling the light inside the device and improving sensor performance. It is possible to prevent a decrease in operating accuracy.
- the material to which the adhesive sheet disclosed herein is attached is not particularly limited, but includes, for example, copper, silver, gold, iron, tin, palladium, aluminum, nickel, titanium, and chromium. , zinc, etc., or metal materials such as alloys containing two or more of these, such as polyimide resins, acrylic resins, polyether nitrile resins, polyether sulfone resins, polyester resins (PET resins, polyethylene resins, etc.).
- polyvinyl chloride resins polyphenylene sulfide resins, polyetheretherketone resins, polyamide resins (so-called aramid resins, etc.), polyarylate resins, polycarbonate resins, liquid crystal polymers, etc. (typically plastic materials), alumina, zirconia, soda glass, quartz glass, carbon, and other inorganic materials.
- metal materials such as copper, aluminum, and stainless steel, and resin materials (typically plastic materials)
- polyester resins such as PET, polyimide resins, aramid resins, and polyphenylene sulfide resins are widely used. ing.
- the above-mentioned material may be a material of a member constituting a product such as an electronic device.
- the adhesive sheet disclosed herein can be used by being attached to a member made of the above material.
- the above-mentioned material may be a material constituting the fixed object (for example, a back member such as an electromagnetic wave shield or a reinforcing plate) such as the pressure-sensitive sensor and the display section.
- the object to be fixed refers to an object to which the adhesive sheet is attached, that is, an adherend.
- the back surface member refers to a member disposed on the opposite side of the pressure-sensitive sensor and the front surface (viewing side) of the display section in, for example, a portable electronic device, and for example, the display device shown in FIG. 4 described below. It may be a member constituting the support portion 540 disposed on the back surface of the device 500 .
- the object to be fixed may have either a single-layer structure or a multi-layer structure, and the surface to which the adhesive sheet is attached (attached surface) may be subjected to various surface treatments.
- an example of the object to be fixed is a back member with a thickness of 1 ⁇ m or more (typically 5 ⁇ m or more, e.g. 60 ⁇ m or more, even 120 ⁇ m or more) and 1500 ⁇ m or less (e.g. 800 ⁇ m or less). Can be mentioned.
- the member or material to which the pressure-sensitive adhesive sheet is attached may be light-transparent (light-transparent adherend). Since the adhesive surface of the adhesive sheet attached to the light-transparent adherend can be visually recognized through the light-transparent adherend, it is desirable that the adhesive surface has good appearance quality.
- the light transmittance of the light-transmitting adherend may be, for example, greater than 50%, and may be 70% or more. In some preferred embodiments, the light transmittance of the adherend is 80% or more, more preferably 90% or more, and may be 95% or more (for example, 95 to 100%).
- Such a material may be a resin film (for example, a polyester resin film such as a PET film) placed on the back surface of an image display section of various devices such as portable electronic devices.
- the pressure-sensitive adhesive sheet disclosed herein can be preferably used in an embodiment in which it is attached to an adherend (for example, a member) having a light transmittance of a predetermined value or more as described above.
- the above-mentioned light transmittance is a light transmittance at a wavelength of 550 nm, and can be measured in the same manner as the light transmittance at a wavelength of 550 nm of the pressure-sensitive adhesive sheet.
- the adhesive sheet is used in a manner in which it is attached to a metal member.
- the material of the metal member include the metal materials exemplified as the adherend material.
- a metal member is, for example, a member or article having a surface (adhesive sheet pasting surface) made of a metal material such as aluminum or stainless steel, and a preferable example is a metal member such as a stainless steel member or an aluminum member. Examples include members.
- the adhesive sheet may cover the entire surface of the metal member, or may cover a portion of the surface (for example, a partial area where concealment is required).
- the metal member may be, for example, a member that constitutes a support portion 540 of a display device 500 shown in FIG. 4, which will be described later.
- the metal member is preferably one adherend of the adhesive sheet.
- a laminate including an adhesive sheet and a member to which the adhesive sheet is attached is provided.
- a laminate including an adhesive sheet is a laminate including the adhesive sheet and a metal member (first member).
- Such a laminate may include a metal member and an adhesive sheet that covers at least a portion of the surface of the metal member.
- the adhesive sheet may cover the entire surface of the metal member, or may cover a portion of the surface (for example, a partial area where concealment is required).
- one surface (adhesive surface) of the adhesive sheet is attached to the metal member.
- the member to which the adhesive sheet is attached may have the light transmittance of the adherend material described above.
- the laminate including the adhesive sheet is a laminate including the adhesive sheet and a light-transmitting member (second member).
- the laminate includes a metal member (first member), an adhesive sheet (specifically, a double-sided adhesive sheet), and a light-transmitting member (second member). This is a laminate provided in this order.
- the base material-less double-sided adhesive sheet is also referred to as an adhesive layer in the laminate.
- the laminate 50 shown in FIG. 3 includes a first member 41, an adhesive sheet 1, and a second member 42 in this order.
- the adhesive sheet 1 is configured as a double-sided adhesive sheet without a base material.
- one adhesive surface (first adhesive surface) 1A of the base material-less double-sided adhesive sheet 1 is adhered to the first member 41, and the other adhesive surface of the double-sided adhesive sheet 1 is adhered to the first member 41.
- the surface (second adhesive surface) 1B is adhered to the second member 42.
- both the first member 41 and the second member 42 have a sheet-like or plate-like shape, and the laminate 50 has a multilayer structure.
- the first member 41 is a metal member
- the second member 42 is a light-transmitting member.
- the details of the members constituting the laminate are the same as those described above for the members, materials, and adherends, so duplicate explanations will not be repeated.
- the adhesive sheet is preferably used in electronic devices that include various light sources such as LEDs (light emitting diodes) and light emitting elements such as self-luminous organic EL.
- various light sources such as LEDs (light emitting diodes) and light emitting elements such as self-luminous organic EL.
- it can be preferably used in electronic equipment (typically portable electronic equipment) that includes an organic EL display device or a liquid crystal display device that requires predetermined optical properties.
- FIG. 4 is an exploded perspective view schematically showing an example of the configuration of the display device.
- the display device 500 included in the portable electronic device 400 includes a display section 520 including a cover member, an organic EL unit, etc., and a support section 540.
- the display device 500 is configured to further include an adhesive sheet 530.
- the adhesive sheet 530 fixes the members that constitute the display section 520 and the support section 540.
- the support portion 540 includes a substrate (a metal plate such as a stainless steel plate or an aluminum plate), and the like.
- the adhesive sheet disclosed herein is preferably used as a component of the above display device.
- the adhesive sheet disclosed herein may have an adhesive layer containing an acrylic polymer with a high biomass carbon ratio in some embodiments, conventional general acrylic adhesives (i.e. By being used as a substitute for acrylic adhesives in various applications where acrylic adhesives (acrylic adhesives with a low biomass carbon ratio) are used, it can contribute to reducing dependence on fossil resource-based materials.
- the adhesive sheet disclosed herein can be preferably used as an adhesive sheet with reduced dependence on fossil resource materials.
- a display device including a display section including a cover member and an organic EL unit, and a support section, An adhesive sheet is bonded to the support portion, The adhesive sheet has a colored adhesive layer, The adhesive layer includes an acrylic polymer, The adhesive layer has a gel fraction of 25% or more, The adhesive layer has a storage elastic modulus of 0.05 MPa or more at 23°C, and a tan ⁇ of 0.31 or more at 23°C, where the tan ⁇ is the storage elasticity of the adhesive layer.
- a display device that refers to the ratio of the loss modulus G'' to the modulus G'(G''/G').
- a pressure-sensitive adhesive sheet having a colored pressure-sensitive adhesive layer The adhesive layer includes an acrylic polymer, The adhesive layer has a gel fraction of 25% or more, The adhesive layer has a storage elastic modulus of 0.05 MPa or more at 23°C, and a tan ⁇ of 0.31 or more at 23°C, where the tan ⁇ is the storage elasticity of the adhesive layer.
- Adhesive sheet refers to the ratio of loss elastic modulus G'' to modulus G'(G''/G').
- a pressure-sensitive adhesive sheet with a release liner comprising the pressure-sensitive adhesive sheet according to any one of [11] to [20] above, and a release liner laminated on the adhesive surface of the pressure-sensitive adhesive sheet.
- a laminate comprising a metal member (first member) and an adhesive sheet,
- the adhesive sheet has a colored adhesive layer,
- the adhesive layer includes an acrylic polymer,
- the adhesive layer has a gel fraction of 25% or more,
- the adhesive layer has a storage elastic modulus of 0.05 MPa or more at 23°C, and a tan ⁇ of 0.31 or more at 23°C, where the tan ⁇ is the storage elasticity of the adhesive layer.
- a laminate which refers to the ratio of the loss modulus G'' to the modulus G'(G''/G').
- a laminate comprising a light-transmitting member (second member) and an adhesive sheet,
- the adhesive sheet has a colored adhesive layer
- the adhesive layer includes an acrylic polymer
- the adhesive layer has a gel fraction of 25% or more
- the adhesive layer has a storage elastic modulus of 0.05 MPa or more at 23°C, and a tan ⁇ of 0.31 or more at 23°C, where the tan ⁇ is the storage elasticity of the adhesive layer.
- a laminate which refers to the ratio of the loss modulus G'' to the modulus G'(G''/G').
- a laminate comprising a metal member (first member), an adhesive sheet, and a light-transmitting member (second member) in this order,
- the adhesive sheet has a colored adhesive layer
- the adhesive layer includes an acrylic polymer
- the adhesive layer has a gel fraction of 25% or more
- the adhesive layer has a storage elastic modulus of 0.05 MPa or more at 23°C, and a tan ⁇ of 0.31 or more at 23°C, where the tan ⁇ is the storage elasticity of the adhesive layer.
- a laminate which refers to the ratio of the loss modulus G'' to the modulus G'(G''/G').
- n-HpA is a compound having a biomass-derived heptyl group at the ester end, which was synthesized using biomass-derived heptyl alcohol.
- terpene phenol resin tackifier resin
- tackifier resin the trade name "YS Polyster T-115" (manufactured by Yasuhara Chemical Co., Ltd., softening point: about 115°C, hydroxyl value: 30 to 60 mgKOH/g) was used.
- isocyanate-based crosslinking agent A the product name "Coronate L” (manufactured by Tosoh Corporation, 75% ethyl acetate solution of trimethylolpropane/tolylene diisocyanate trimer adduct) was used.
- epoxy crosslinking agent the trade name "TETRAD-C” (manufactured by Mitsubishi Gas Chemical Co., Ltd., 1,3-bis(N,N-diglycidylaminomethyl)cyclohexane) was used.
- carbon black particles the product name "Multilac A903” (manufactured by Toyo Color Co., Ltd., carbon black particle dispersion, average particle size 400 nm) was used.
- acrylic oligomer one prepared by the following method was used.
- the obtained adhesive composition was applied to the release surface of a 38 ⁇ m thick polyester release liner (trade name "Diafoil MRF", manufactured by Mitsubishi Chemical Corporation) and dried at 100° C. for 2 minutes to form a 35 ⁇ m thick polyester release liner. An adhesive layer was formed. A release surface of a polyester release liner (trade name "Diafoil MRF", manufactured by Mitsubishi Chemical Corporation) having a thickness of 25 ⁇ m was attached to this adhesive layer. In this way, a base material-less double-sided pressure-sensitive adhesive sheet with a release liner was obtained, both sides of which were protected by the two polyester release liners.
- Examples 2 to 8 and Comparative Examples 1 to 4> The monomer composition of the acrylic polymer, the type and amount of colorant in the adhesive layer, the amount of tackifying resin, the amount of acrylic oligomer, the type and amount of crosslinking agent, and the adhesive layer thickness are as shown in Table 1.
- a pressure-sensitive adhesive composition according to each example was prepared in the same manner as in Example 1 except for the changes, and a double-sided pressure-sensitive adhesive sheet with a release liner according to each example was produced using the pressure-sensitive adhesive composition.
- BA represents n-butyl acrylate.
- isocyanate-based crosslinking agent B represents an isocyanurate form of hexamethylene diisocyanate (manufactured by Tosoh Corporation, trade name "Coronate HX", 1% ethyl acetate solution of a trifunctional isocyanate compound), and is shown in Table 1.
- the content shown represents the content of solid content (non-volatile content).
- the white colorant represents titanium oxide (TiO 2 ) particles (product name "WHITE PASTE R-2228", manufactured by Dainichiseika Kagyo Co., Ltd., average particle size 50 nm).
- the double-sided adhesive sheet with a release liner according to each example (a laminate of a release liner on a light release side/a double-sided adhesive sheet/a release liner on a heavy release side) is wound in the same environment and under the same conditions to form a roll body, After a predetermined period of time had elapsed, the material unwound from the roll was cut into a size of 500 mm x 1000 mm to obtain a sample for evaluation.
- the back side of the release liner on the heavy release side was wiped with Kimwipe (manufactured by Nippon Paper Crecia Co., Ltd.) to remove foreign matter, and then the release liner on the light release side was peeled from the evaluation sample.
- the evaluation sample was held in a flat shape at the midpoint between the point light source and the projection screen, which were arranged at a distance of about 100 cm (a position at a distance of about 50 cm from the point light source), The evaluation sample was arranged so that the angle of the exposed pressure-sensitive adhesive layer surface to the light beam from the point light source was about 90 degrees.
- the surface of the adhesive layer from which the release liner on the easy-release side was peeled off was placed on the point light source side.
- the point light source was turned on and the image projected onto the screen through the evaluation sample was visually observed to determine the uneven deformation (specifically, The presence or absence of uneven deformation on the surface of the adhesive layer was evaluated.
- a point light source for example, "xenon lamp C2577" manufactured by Hamamatsu Photonics Co., Ltd. can be used.
- the adhesives according to Examples 1 to 8 are colored, contain an acrylic polymer, have a gel fraction of 25% or more, a 23°C storage modulus of 0.05 MPa or more, and a 23°C storage modulus of 0.05 MPa or more.
- the pressure-sensitive adhesive sheet containing the above-mentioned pressure-sensitive adhesive having a tan ⁇ of 0.31 or more had a passing score of 8/10 or higher in the unevenness deformation evaluation.
- Comparative Example 1 in which the adhesive had a storage modulus of elasticity at 23° C. of less than 0.05 MPa, the results of the unevenness deformation evaluation were inferior to Examples 1 to 8.
- Comparative Example 2 in which the 23° C.
- Comparative Example 3 in which the 23° C. tan ⁇ was even lower than Comparative Example 2, had even worse results. Furthermore, Comparative Example 4 in which the adhesive had a gel fraction of less than 25% also had a poor evaluation of unevenness deformation. In Comparative Examples 1 and 4, relatively large uneven deformation occurred because the 23° C. storage modulus or gel fraction was low, and it is thought that this appeared in the evaluation results. The evaluation results of Comparative Examples 2 and 3 are considered to be due to the fact that the uneven deformation that occurred in the adhesive layer was not sufficiently alleviated, and fine uneven deformation remained.
Landscapes
- Chemical & Material Sciences (AREA)
- Organic Chemistry (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Inorganic Chemistry (AREA)
- Health & Medical Sciences (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Adhesive Tapes (AREA)
- Adhesives Or Adhesive Processes (AREA)
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202280068989.2A CN118119679A (zh) | 2022-09-13 | 2022-12-12 | 粘合片 |
| KR1020257011992A KR102942787B1 (ko) | 2022-09-13 | 2022-12-12 | 점착 시트 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2022-145689 | 2022-09-13 | ||
| JP2022145689A JP7321344B1 (ja) | 2022-09-13 | 2022-09-13 | 粘着シート |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2024057560A1 true WO2024057560A1 (ja) | 2024-03-21 |
Family
ID=87474521
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2022/045742 Ceased WO2024057560A1 (ja) | 2022-09-13 | 2022-12-12 | 粘着シート |
Country Status (4)
| Country | Link |
|---|---|
| JP (2) | JP7321344B1 (cg-RX-API-DMAC7.html) |
| KR (1) | KR102942787B1 (cg-RX-API-DMAC7.html) |
| CN (1) | CN118119679A (cg-RX-API-DMAC7.html) |
| WO (1) | WO2024057560A1 (cg-RX-API-DMAC7.html) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2026134268A1 (ja) * | 2024-12-20 | 2026-06-25 | 東亞合成株式会社 | 粘着剤組成物、粘着シート、加飾フィルム及び加飾成形体 |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2026155188A1 (ja) * | 2025-01-17 | 2026-07-23 | 株式会社レゾナック | 接着剤組成物及び接着体 |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2020164615A (ja) * | 2019-03-29 | 2020-10-08 | 日東電工株式会社 | 粘着シート |
| WO2021125247A1 (ja) * | 2019-12-18 | 2021-06-24 | 積水化学工業株式会社 | 粘着剤、粘着テープ、電化製品、車載部材、及び固定方法 |
| JP2022125728A (ja) * | 2021-02-17 | 2022-08-29 | リンテック株式会社 | 粘着剤および粘着シート |
| JP2023003416A (ja) * | 2021-06-23 | 2023-01-11 | 積水化学工業株式会社 | 粘着テープ、電化製品、車載部材及び固定方法 |
| JP2023008802A (ja) * | 2021-07-06 | 2023-01-19 | 日東電工株式会社 | 両面粘着シート |
Family Cites Families (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5219359B2 (ja) * | 2006-02-21 | 2013-06-26 | 日東電工株式会社 | 反射性及び/又は遮光性を有する粘着テープ又はシート、および液晶表示装置 |
| JP6381950B2 (ja) * | 2013-06-25 | 2018-08-29 | 日東電工株式会社 | 粘着剤組成物、表面保護フィルム、及び、光学部材 |
| CN105518094B (zh) * | 2013-09-10 | 2019-04-05 | 积水化学工业株式会社 | 电子设备用粘合片 |
| JP6513347B2 (ja) * | 2014-07-07 | 2019-05-15 | 日東電工株式会社 | 粘着シート |
| JP2016044203A (ja) * | 2014-08-20 | 2016-04-04 | 株式会社クラレ | アクリル系粘着剤組成物及び粘着製品 |
| JP6673446B1 (ja) * | 2018-11-16 | 2020-03-25 | 王子ホールディングス株式会社 | 透明部材貼合用粘着シート |
| JP6743855B2 (ja) | 2018-09-05 | 2020-08-19 | 王子ホールディングス株式会社 | 光学部材貼合用粘着シート及び積層体の製造方法 |
| JP7193401B2 (ja) * | 2019-03-28 | 2022-12-20 | 日東電工株式会社 | 粘着剤組成物、粘着剤層、及び粘着シート |
| JP7339009B2 (ja) * | 2019-03-29 | 2023-09-05 | 日東電工株式会社 | 粘着シート |
| JP2020164764A (ja) * | 2019-03-29 | 2020-10-08 | 株式会社巴川製紙所 | 着色粘着剤と、それを用いた着色粘着積層シート |
| EP4079823A4 (en) * | 2019-12-18 | 2023-08-02 | Sekisui Chemical Co., Ltd. | Adhesive agent composition, adhesive tape, affixing method for electronic device component or in-vehicle component, and production method for electronic device component or in-vehicle component |
| JP7798467B2 (ja) * | 2020-03-24 | 2026-01-14 | 日東電工株式会社 | 粘着シート |
| JP6945091B1 (ja) * | 2020-08-31 | 2021-10-06 | 日東電工株式会社 | 粘着シート、表示装置、構造体および光透過性部材付き粘着シート |
| JP7878862B2 (ja) * | 2020-09-14 | 2026-06-23 | 日東電工株式会社 | 粘着シート |
| JP7128389B1 (ja) * | 2021-03-22 | 2022-08-30 | 積水化学工業株式会社 | 粘着テープ、電子機器部品又は車載機器部品の固定方法、及び、電子機器又は車載機器の製造方法 |
-
2022
- 2022-09-13 JP JP2022145689A patent/JP7321344B1/ja active Active
- 2022-12-12 WO PCT/JP2022/045742 patent/WO2024057560A1/ja not_active Ceased
- 2022-12-12 CN CN202280068989.2A patent/CN118119679A/zh active Pending
- 2022-12-12 KR KR1020257011992A patent/KR102942787B1/ko active Active
-
2023
- 2023-07-25 JP JP2023120708A patent/JP2024041043A/ja active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2020164615A (ja) * | 2019-03-29 | 2020-10-08 | 日東電工株式会社 | 粘着シート |
| WO2021125247A1 (ja) * | 2019-12-18 | 2021-06-24 | 積水化学工業株式会社 | 粘着剤、粘着テープ、電化製品、車載部材、及び固定方法 |
| JP2022125728A (ja) * | 2021-02-17 | 2022-08-29 | リンテック株式会社 | 粘着剤および粘着シート |
| JP2023003416A (ja) * | 2021-06-23 | 2023-01-11 | 積水化学工業株式会社 | 粘着テープ、電化製品、車載部材及び固定方法 |
| JP2023008802A (ja) * | 2021-07-06 | 2023-01-19 | 日東電工株式会社 | 両面粘着シート |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2026134268A1 (ja) * | 2024-12-20 | 2026-06-25 | 東亞合成株式会社 | 粘着剤組成物、粘着シート、加飾フィルム及び加飾成形体 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2024041000A (ja) | 2024-03-26 |
| CN118119679A (zh) | 2024-05-31 |
| JP2024041043A (ja) | 2024-03-26 |
| KR20250065407A (ko) | 2025-05-12 |
| JP7321344B1 (ja) | 2023-08-04 |
| KR102942787B1 (ko) | 2026-03-24 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6774806B2 (ja) | 粘着シート | |
| JP6945091B1 (ja) | 粘着シート、表示装置、構造体および光透過性部材付き粘着シート | |
| JP7339009B2 (ja) | 粘着シート | |
| JP7537876B2 (ja) | 粘着シートおよび粘着剤組成物 | |
| WO2022054787A1 (ja) | 粘着シート | |
| JP2024041043A (ja) | 粘着シート | |
| JP7523224B2 (ja) | 粘着シート | |
| JP7087162B2 (ja) | 粘着シート | |
| JP6884258B1 (ja) | 粘着シート | |
| JP7321342B1 (ja) | 剥離ライナー付き両面粘着シート | |
| JP7558659B2 (ja) | 粘着シート | |
| JP7321343B1 (ja) | 両面粘着シート | |
| WO2023074447A1 (ja) | 粘着シート、剥離ライナー付き粘着シートおよび積層体 | |
| WO2022249726A1 (ja) | 粘着シート、表示装置および積層体 | |
| WO2023027091A1 (ja) | 積層体 | |
| WO2023027092A1 (ja) | 積層体 | |
| WO2022249727A1 (ja) | 粘着シート、表示装置および積層体 | |
| WO2022264861A1 (ja) | 粘着シート、表示装置および積層体 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 202280068989.2 Country of ref document: CN |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 22958877 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 20257011992 Country of ref document: KR Kind code of ref document: A |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1020257011992 Country of ref document: KR |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 22958877 Country of ref document: EP Kind code of ref document: A1 |