WO2022172448A1 - 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 - Google Patents
二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 Download PDFInfo
- Publication number
- WO2022172448A1 WO2022172448A1 PCT/JP2021/005515 JP2021005515W WO2022172448A1 WO 2022172448 A1 WO2022172448 A1 WO 2022172448A1 JP 2021005515 W JP2021005515 W JP 2021005515W WO 2022172448 A1 WO2022172448 A1 WO 2022172448A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- film
- polyol
- polyisocyanate
- composition
- coating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/28—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the compounds used containing active hydrogen
- C08G18/40—High-molecular-weight compounds
- C08G18/48—Polyethers
- C08G18/4825—Polyethers containing two hydroxy groups
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B27/00—Layered products comprising a layer of synthetic resin
- B32B27/06—Layered products comprising a layer of synthetic resin as the main or only constituent of a layer, which is next to another layer of the same or of a different material
- B32B27/08—Layered products comprising a layer of synthetic resin as the main or only constituent of a layer, which is next to another layer of the same or of a different material of synthetic resin
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B27/00—Layered products comprising a layer of synthetic resin
- B32B27/16—Layered products comprising a layer of synthetic resin specially treated, e.g. irradiated
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B27/00—Layered products comprising a layer of synthetic resin
- B32B27/32—Layered products comprising a layer of synthetic resin comprising polyolefins
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B27/00—Layered products comprising a layer of synthetic resin
- B32B27/36—Layered products comprising a layer of synthetic resin comprising polyesters
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B7/00—Layered products characterised by the relation between layers; Layered products characterised by the relative orientation of features between layers, or by the relative values of a measurable parameter between layers, i.e. products comprising layers having different physical, chemical or physicochemical properties; Layered products characterised by the interconnection of layers
- B32B7/04—Interconnection of layers
- B32B7/12—Interconnection of layers using interposed adhesives or interposed materials with bonding properties
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/08—Processes
- C08G18/10—Prepolymer processes involving reaction of isocyanates or isothiocyanates with compounds having active hydrogen in a first reaction step
- C08G18/12—Prepolymer processes involving reaction of isocyanates or isothiocyanates with compounds having active hydrogen in a first reaction step using two or more compounds having active hydrogen in the first polymerisation step
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/08—Processes
- C08G18/16—Catalysts
- C08G18/18—Catalysts containing secondary or tertiary amines or salts thereof
- C08G18/20—Heterocyclic amines; Salts thereof
- C08G18/2009—Heterocyclic amines; Salts thereof containing one heterocyclic ring
- C08G18/2018—Heterocyclic amines; Salts thereof containing one heterocyclic ring having one nitrogen atom in the ring
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/08—Processes
- C08G18/16—Catalysts
- C08G18/22—Catalysts containing metal compounds
- C08G18/227—Catalysts containing metal compounds of antimony, bismuth or arsenic
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/08—Processes
- C08G18/16—Catalysts
- C08G18/22—Catalysts containing metal compounds
- C08G18/24—Catalysts containing metal compounds of tin
- C08G18/244—Catalysts containing metal compounds of tin tin salts of carboxylic acids
- C08G18/246—Catalysts containing metal compounds of tin tin salts of carboxylic acids containing also tin-carbon bonds
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/28—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the compounds used containing active hydrogen
- C08G18/2805—Compounds having only one group containing active hydrogen
- C08G18/288—Compounds containing at least one heteroatom other than oxygen or nitrogen
- C08G18/289—Compounds containing at least one heteroatom other than oxygen or nitrogen containing silicon
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/28—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the compounds used containing active hydrogen
- C08G18/30—Low-molecular-weight compounds
- C08G18/32—Polyhydroxy compounds; Polyamines; Hydroxyamines
- C08G18/3203—Polyhydroxy compounds
- C08G18/3206—Polyhydroxy compounds aliphatic
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/28—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the compounds used containing active hydrogen
- C08G18/30—Low-molecular-weight compounds
- C08G18/32—Polyhydroxy compounds; Polyamines; Hydroxyamines
- C08G18/3271—Hydroxyamines
- C08G18/3278—Hydroxyamines containing at least three hydroxy groups
- C08G18/3281—Hydroxyamines containing at least three hydroxy groups containing three hydroxy groups
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/28—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the compounds used containing active hydrogen
- C08G18/30—Low-molecular-weight compounds
- C08G18/32—Polyhydroxy compounds; Polyamines; Hydroxyamines
- C08G18/3271—Hydroxyamines
- C08G18/3278—Hydroxyamines containing at least three hydroxy groups
- C08G18/3284—Hydroxyamines containing at least three hydroxy groups containing four hydroxy groups
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/28—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the compounds used containing active hydrogen
- C08G18/40—High-molecular-weight compounds
- C08G18/48—Polyethers
- C08G18/50—Polyethers having heteroatoms other than oxygen
- C08G18/5021—Polyethers having heteroatoms other than oxygen having nitrogen
- C08G18/5024—Polyethers having heteroatoms other than oxygen having nitrogen containing primary and/or secondary amino groups
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/70—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the isocyanates or isothiocyanates used
- C08G18/72—Polyisocyanates or polyisothiocyanates
- C08G18/721—Two or more polyisocyanates not provided for in one single group C08G18/73 - C08G18/80
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/70—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the isocyanates or isothiocyanates used
- C08G18/72—Polyisocyanates or polyisothiocyanates
- C08G18/74—Polyisocyanates or polyisothiocyanates cyclic
- C08G18/76—Polyisocyanates or polyisothiocyanates cyclic aromatic
- C08G18/7614—Polyisocyanates or polyisothiocyanates cyclic aromatic containing only one aromatic ring
- C08G18/7628—Polyisocyanates or polyisothiocyanates cyclic aromatic containing only one aromatic ring containing at least one isocyanate or isothiocyanate group linked to the aromatic ring by means of an aliphatic group
- C08G18/7642—Polyisocyanates or polyisothiocyanates cyclic aromatic containing only one aromatic ring containing at least one isocyanate or isothiocyanate group linked to the aromatic ring by means of an aliphatic group containing at least two isocyanate or isothiocyanate groups linked to the aromatic ring by means of an aliphatic group having a primary carbon atom next to the isocyanate or isothiocyanate groups, e.g. xylylene diisocyanate or homologues substituted on the aromatic ring
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G18/00—Polymeric products of isocyanates or isothiocyanates
- C08G18/06—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen
- C08G18/70—Polymeric products of isocyanates or isothiocyanates with compounds having active hydrogen characterised by the isocyanates or isothiocyanates used
- C08G18/72—Polyisocyanates or polyisothiocyanates
- C08G18/74—Polyisocyanates or polyisothiocyanates cyclic
- C08G18/76—Polyisocyanates or polyisothiocyanates cyclic aromatic
- C08G18/7657—Polyisocyanates or polyisothiocyanates cyclic aromatic containing two or more aromatic rings
- C08G18/7664—Polyisocyanates or polyisothiocyanates cyclic aromatic containing two or more aromatic rings containing alkylene polyphenyl groups
- C08G18/7671—Polyisocyanates or polyisothiocyanates cyclic aromatic containing two or more aromatic rings containing alkylene polyphenyl groups containing only one alkylene bisphenyl group
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J175/00—Adhesives based on polyureas or polyurethanes; Adhesives based on derivatives of such polymers
- C09J175/04—Polyurethanes
- C09J175/08—Polyurethanes from polyethers
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J175/00—Adhesives based on polyureas or polyurethanes; Adhesives based on derivatives of such polymers
- C09J175/04—Polyurethanes
- C09J175/12—Polyurethanes from compounds containing nitrogen and active hydrogen, the nitrogen atom not being part of an isocyanate group
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J5/00—Adhesive processes in general; Adhesive processes not provided for elsewhere, e.g. relating to primers
- C09J5/04—Adhesive processes in general; Adhesive processes not provided for elsewhere, e.g. relating to primers involving separate application of adhesive ingredients to the different surfaces to be joined
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2250/00—Layers arrangement
- B32B2250/02—2 layers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2250/00—Layers arrangement
- B32B2250/24—All layers being polymeric
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
- B32B2255/10—Coating on the layer surface on synthetic resin layer or on natural or synthetic rubber layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
- B32B2255/20—Inorganic coating
- B32B2255/205—Metallic coating
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2255/00—Coating on the layer surface
- B32B2255/26—Polymeric coating
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2323/00—Polyalkenes
- B32B2323/10—Polypropylene
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B2367/00—Polyesters, e.g. PET, i.e. polyethylene terephthalate
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B37/00—Methods or apparatus for laminating, e.g. by curing or by ultrasonic bonding
- B32B37/12—Methods or apparatus for laminating, e.g. by curing or by ultrasonic bonding characterised by using adhesives
- B32B37/1284—Application of adhesive
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B37/00—Methods or apparatus for laminating, e.g. by curing or by ultrasonic bonding
- B32B37/14—Methods or apparatus for laminating, e.g. by curing or by ultrasonic bonding characterised by the properties of the layers
- B32B37/16—Methods or apparatus for laminating, e.g. by curing or by ultrasonic bonding characterised by the properties of the layers with all layers existing as coherent layers before laminating
- B32B37/20—Methods or apparatus for laminating, e.g. by curing or by ultrasonic bonding characterised by the properties of the layers with all layers existing as coherent layers before laminating involving the assembly of continuous webs only
- B32B37/203—One or more of the layers being plastic
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J2301/00—Additional features of adhesives in the form of films or foils
- C09J2301/30—Additional features of adhesives in the form of films or foils characterized by the chemical, physicochemical or physical properties of the adhesive or the carrier
- C09J2301/312—Additional features of adhesives in the form of films or foils characterized by the chemical, physicochemical or physical properties of the adhesive or the carrier parameters being the characterizing feature
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09J—ADHESIVES; NON-MECHANICAL ASPECTS OF ADHESIVE PROCESSES IN GENERAL; ADHESIVE PROCESSES NOT PROVIDED FOR ELSEWHERE; USE OF MATERIALS AS ADHESIVES
- C09J2475/00—Presence of polyurethane
Definitions
- the present invention relates to a two-component curing adhesive, a laminated film, a laminated film manufacturing apparatus, and a laminated film manufacturing method.
- a laminate film in which two films are bonded together using an adhesive, and a two-component curing adhesive that uses a curing reaction between a polyisocyanate composition and a polyol composition is used as the adhesive.
- a method for producing a laminated film using a two-component curing adhesive there are a method having a two-component mixed coating process that has been used for a long time and a method having a two-component separate coating process that has been attracting attention in recent years.
- the polyisocyanate composition and the polyol composition are mixed to form a mixed liquid, and the two-liquid mixing coating step of applying this on the film, and the coating film formed on the film. and a step of forming an adhesive layer in which another film is laminated and cured.
- a two-component separated coating comprising a first coating step of coating the polyisocyanate composition on the first film and a second coating step of coating the polyol composition on the second film.
- Patent Documents 1 to 3 disclose solvent-free agent A that is liquid at room temperature applied to one adherend and solvent-free agent B that is liquid at room temperature and applied to the other adherend.
- a two-part split-coat adhesive is described that initiates a curing reaction when it comes into contact with the adhesive.
- the above agent A is mainly composed of a compound having an isocyanate group at both ends of the molecule
- the above agent B is a compound having an amino group at both ends of the molecule and a compound having a tertiary amine in the molecule. and a tackifying resin are described.
- the A agent is mainly composed of a compound having an isocyanate group at both molecular ends
- the B agent is a two-component separate application type mainly composed of a compound having an amino group at both molecular ends.
- a urethane adhesive is described.
- the A agent is mainly composed of a compound having an isocyanate group at both ends of the molecule
- the B agent is a two-liquid separate application type urethane system mainly composed of a compound having a hydroxyl group in the molecule. Adhesives are mentioned.
- the cohesive force (initial cohesive force) immediately after adhesion may be insufficient.
- the aging process may take a long time, or heating at about 40 to 60° C. may be required. For this reason, there was a possibility that the production efficiency of the laminated film would be lowered.
- contact between the substrates occurs for the first time after the polyisocyanate composition and the polyol composition are each coated. For this reason, mixing of the composition and reaction between functional groups in the composition occur slowly, often resulting in insufficient initial cohesive strength.
- misting stringing phenomenon
- the adhesive scatters and adheres to manufacturing equipment and facilities, requiring periodic shutdown and cleaning.
- the rotation speed of the rolls and the transport speed of the film are lowered in order to reduce the occurrence of misting, the production efficiency is lowered.
- misting of the two-component curable adhesive tends to occur when the film transport speed is increased, which poses a problem. rice field.
- the present invention has been made in view of the above circumstances, and is a two-component curing adhesive that uses a curing reaction between a polyisocyanate composition and a polyol composition, has excellent initial cohesive strength, and To provide a two-liquid curable adhesive that hardly causes misting even in a coating step.
- the present invention is a two-component curable adhesive that uses a curing reaction between a polyisocyanate composition and a polyol composition, which hardly generates misting even when the step of coating on a film is performed, and has excellent initial cohesive strength.
- An object of the present invention is to provide a laminated film which can be produced efficiently by using a two-component curing adhesive and which has excellent properties.
- the present invention uses a two-component curable adhesive that is resistant to misting and has excellent initial cohesive strength, using a curing reaction between a polyisocyanate composition and a polyol composition, and a production method having a two-component separate application step.
- An object of the present invention is to provide a laminated film manufacturing apparatus that can be suitably used when manufacturing a laminated film by a method.
- the present invention uses a two-component curing adhesive that is resistant to misting and has excellent initial cohesive strength, using a curing reaction between a polyisocyanate composition and a polyol composition, to efficiently produce a laminated film. It aims at providing the manufacturing method of.
- the present inventors have found that when using a two-component curing adhesive that uses a curing reaction between a polyisocyanate composition and a polyol composition, the misting that occurs in the process of applying it to the film In order to suppress the occurrence of this, and to increase the initial cohesive strength of the adhesive, we have made extensive studies. As a result, it was found that by using a polyisocyanate composition and a polyol composition having an elongational viscosity of 0.1 to 10 Pa s, the initial cohesive force can be improved and the occurrence of misting can be suppressed. I came up with That is, the present invention relates to the following matters.
- the polyisocyanate composition (X) contains a polyisocyanate (A)
- the polyol composition (Y) contains a polyol (B)
- a two-component curing adhesive, wherein the polyisocyanate composition (X) and the polyol composition (Y) have extensional viscosities of 0.1 to 10 Pa ⁇ s.
- [2] having an adhesive layer between the first film and the second film; A laminated film, wherein the adhesive layer is a cured product of the two-component curing adhesive according to [1].
- a first coating section that applies a polyisocyanate composition (X) containing a polyisocyanate (A) and having an elongational viscosity of 0.1 to 10 Pa s to the first film; a second coating section for coating a second film with a polyol composition (Y) containing a polyol (B) and having an extensional viscosity of 0.1 to 10 Pa s;
- An apparatus for producing a laminated film comprising a lamination device for laminating the surface of the first film coated with the polyisocyanate composition (X) and the surface of the second film coated with the polyol composition (Y).
- the two-component curing adhesive of the present invention comprises a polyisocyanate composition (X) having an elongational viscosity of 0.1 to 10 Pa s and a polyol composition (Y) having an elongational viscosity of 0.1 to 10 Pa s. It is a two-component curing adhesive that uses a curing reaction with In the two-component curing adhesive of the present invention, the polyisocyanate composition (X) and the polyol composition (Y) have extensional viscosities of 0.1 to 10 Pa ⁇ s, and are excellent in initial cohesive strength. In addition, misting is less likely to occur even when the process of coating the film is performed.
- the two-component curing adhesive of the present invention can be used when manufacturing a laminated film using a manufacturing method such as a manufacturing method having a two-component mixed coating process and a manufacturing method having a two-component separate coating process. It can be used preferably. In particular, it can be suitably used when a laminated film is continuously produced using a method having a two-part separate coating process.
- the laminated film of the present invention has an adhesive layer between the first film and the second film, and the adhesive layer is made of the cured two-component curable adhesive of the present invention. Since the two-component curing adhesive of the present invention is excellent in initial cohesive strength, it is possible to shorten the aging time in the manufacturing process of the laminated film, widen the selection of processes, and efficiently manufacture the film. In addition, the laminated film of the present invention can be produced using the two-component curing adhesive of the present invention, which hardly causes misting even in the step of coating on the film. Therefore, the laminated film of the present invention can be efficiently manufactured using a manufacturing method including a two-component mixed coating process, a manufacturing method including a two-component separate coating process, and the like.
- the first coating unit applies the polyisocyanate composition (X) having an extensional viscosity of 0.1 to 10 Pa s to the first film
- the second coating The working part applies the polyol composition (Y) having an extensional viscosity of 0.1 to 10 Pa ⁇ s to the second film. Therefore, the laminated film manufacturing apparatus of the present invention can be suitably used when manufacturing a laminated film using the liquid-curable adhesive of the present invention by a manufacturing method having a two-liquid separate coating process.
- the method for producing a laminated film of the present invention has a two-part separate coating step, and in the first coating step, the polyisocyanate composition (X) having an elongational viscosity of 0.1 to 10 Pa s is applied to the first film. Then, in the second coating step, the polyol composition (Y) having an extensional viscosity of 0.1 to 10 Pa ⁇ s is coated on the second film. Therefore, in the method for producing a laminated film of the present invention, a laminated film having excellent properties can be produced with high production efficiency using the two-component curing adhesive of the present invention having excellent initial cohesive strength.
- the two-component curable adhesive of the present invention while suppressing the occurrence of misting due to applying the two-component curable adhesive on the film, it can be efficiently carried out at a continuously high film transport speed. Laminated films can be produced well.
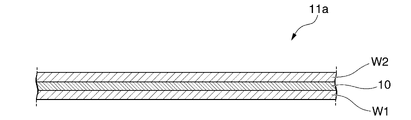
- FIG. 1 is a cross-sectional view showing an example of the laminated film according to this embodiment.
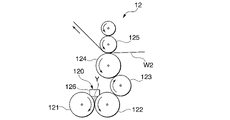
- FIG. 2 is a front view of the laminated film manufacturing apparatus according to the present embodiment.
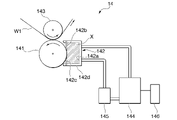
- 3 is a front view showing a main part of a polyol coating section in the laminated film manufacturing apparatus shown in FIG. 2.
- FIG. 4 is a front view showing a main part of a polyisocyanate coating section in the laminated film manufacturing apparatus shown in FIG. 2.
- FIG. FIG. 5 is a front view for explaining another example of the manufacturing apparatus used for manufacturing the laminated film of this embodiment.
- the two-component curable adhesive of the present embodiment is a two-component curable adhesive using a curing reaction between the polyisocyanate composition (X) and the polyol composition (Y).
- the polyisocyanate composition (X) in the two-component curing adhesive of the present embodiment contains the polyisocyanate (A) and has an elongational viscosity of 0.1 to 10 Pa ⁇ s.
- the polyol composition (Y) contains the polyol (B) and has an elongational viscosity of 0.1 to 10 Pa ⁇ s.
- the polyisocyanate composition (X) may contain part of the polyol (B) contained in the two-component curing adhesive, if necessary.
- the two-component curable adhesive of this embodiment cures through a chemical reaction between the isocyanate groups in the polyisocyanate composition (X) and the hydroxyl groups (or hydroxyl groups and amino groups) in the polyol composition (Y).
- the two-component curing adhesive of the present embodiment has an elongational viscosity of 0.1 to 10 Pa ⁇ s for the polyisocyanate composition (X) and the polyol composition (Y), and is excellent in initial cohesive strength.
- the extensional viscosity of the polyisocyanate composition (X) and the polyol composition (Y) is 0.1 to 10 Pa s
- misting stringing phenomenon
- the two-component curable adhesive of the present embodiment can be suitably used particularly when a laminated film is produced using a method having a two-component separate coating process in which misting is likely to occur.
- the polyisocyanate composition (X) having an elongational viscosity of 0.1 to 10 Pa ⁇ s and the polyol composition (Y) having an elongational viscosity of 0.1 to 10 Pa ⁇ s have good reactivity.
- the elongational viscosity of the polyisocyanate composition (X) is preferably 3 Pa s or more, more preferably 5 Pa s or more, more preferably 7 Pa s when a composition containing a prepolymer to be described later is used. It is more preferable that it is above.
- the elongational viscosity of the polyol composition (Y) can more effectively suppress misting and has better reactivity with the polyisocyanate composition (X) to further improve the initial cohesive strength. ⁇ s or less is preferable, 5 Pa ⁇ s or less is more preferable, 3 Pa ⁇ s or less is even more preferable, and 2 Pa ⁇ s or less is particularly preferable. It is also preferable that the elongational viscosity of the polyol composition (Y) is 1 Pa ⁇ s or less.
- Polyisocyanate composition (X) and polyol composition (Y) are preferably applied onto a substrate using a roll coater or gravure coater.
- the polyisocyanate composition (X) and the polyol composition (Y) preferably have a constant elongational viscosity, preferably greater than 0.1 Pa s, and greater than 0.2 Pa s. is more preferable.
- the elongational viscosity of the polyisocyanate composition (X) and the polyol composition (Y) is preferably more than 1 Pa ⁇ s.
- the elongational viscosity of the polyisocyanate composition (X) can be controlled by adjusting the ratio of the low-viscosity material and the high-viscosity material contained in the materials (compounds) used in the polyisocyanate composition (X).
- a person skilled in the art can grasp the viscosity of the material (compound) used for the polyisocyanate composition (X).
- those skilled in the art can combine the materials (compounds) used in the polyisocyanate composition (X) and appropriately adjust the compounding ratio, within the scope of ordinary experiments, based on known techniques, A polyisocyanate composition (X) having an extensional viscosity within the desired range can be obtained.
- the extensional viscosity of the polyol composition (Y) can be controlled by adjusting the ratio of the low-viscosity material and the high-viscosity material contained in the materials (compounds) used in the polyol composition (Y).
- a person skilled in the art can grasp the viscosity of the material (compound) used for the polyol composition (Y). Further, those skilled in the art can combine the materials (compounds) used in the polyol composition (Y) and appropriately adjust the compounding ratio to achieve the desired result within the scope of ordinary experiments based on known techniques.
- a polyol composition (Y) having an extensional viscosity within the range of can be obtained.
- Polyisocyanate (A) As the polyisocyanate (A), known ones can be used without particular limitation.
- Examples of the polyisocyanate (A) include tolylene diisocyanate, 2,4'-diphenylmethane diisocyanate (hereinafter, diphenylmethane diisocyanate may be simply referred to as "MDI"), 2,2'-MDI, 4,4'-MDI, 1,5-naphthalene diisocyanate , aromatic polyisocyanates such as triphenylmethane triisocyanate; Aliphatic polyisocyanates such as xylylene diisocyanate, isophorone diisocyanate, 4,4′-methylenebis(cyclohexyl isocyanate), 1,3-(isocyanatomethyl)cyclohexane, 1,6-hexamethylene diisocyanate, lysine diisocyanate, trimethylhexamethylene diisocyanate ; Compounds in which
- polystyrene resin examples include ethylene glycol, propylene glycol, 1,3-propanediol, 1,4-butanediol, 1 ,5-pentanediol, 3-methyl-1,5-pentanediol, 1,6-hexanediol, neopentyl glycol, methylpentanediol, dimethylbutanediol, butylethylpropanediol, diethylene glycol, triethylene glycol, tetraethylene glycol , dipropylene glycol, tripropylene glycol, bishydroxyethoxybenzene, and other chain aliphatic glycols; 1,4-cyclohexanediol, 1,4-cyclohexanedimethanol, and other alicyclic glycols; g
- a polyester polyol (2) obtained by reacting a polyol such as the linear aliphatic glycol, alicyclic glycol, dimer diol, bisphenol, or polyether polyol with a polyvalent carboxylic acid; polyester polyol (3) obtained by reacting the trifunctional or tetrafunctional aliphatic alcohol with a polycarboxylic acid; A polyester obtained by reacting a polyol such as the chain aliphatic glycol, alicyclic glycol, dimer diol, bisphenol, or polyether polyol, the trifunctional or tetrafunctional aliphatic alcohol, and a polycarboxylic acid.
- Polyester polyol (5) which is a polymer of hydroxy acids such as dimethylolpropionic acid and castor oil fatty acid; Castor oil, dehydrated castor oil, hydrogenated castor oil, castor oil-based polyols such as adducts of 5 to 50 moles of alkylene oxide of castor oil, and mixtures thereof.
- Examples of the polyvalent carboxylic acid used for producing the polyester polyol (2), (3) or (4) include succinic acid, adipic acid, azelaic acid, sebacic acid, dodecanedicarboxylic acid, maleic anhydride, and fumaric acid.
- non-cyclic aliphatic dicarboxylic acids such as; alicyclic dicarboxylic acids such as 1,3-cyclopentanedicarboxylic acid and 1,4-cyclohexanedicarboxylic acid; aromatic dicarboxylic acids such as 2,5-naphthalenedicarboxylic acid, 2,6-naphthalenedicarboxylic acid, naphthalic acid, biphenyldicarboxylic acid, 1,2-bis(phenoxy)ethane-p,p'-dicarboxylic acid; Anhydrides or ester-forming derivatives of aromatic or aromatic dicarboxylic acids; p-hydroxybenzoic acid, p-(2-hydroxyethoxy)benzoic acid and ester-forming derivatives of these dihydroxycarboxylic acids, polybasic acids such as dimer acid is mentioned.
- the polyisocyanate (A1) is preferred, and the polyisocyanate obtained by reacting the polyether polyol and the polyisocyanate is particularly preferred from the viewpoint of wettability. Furthermore, it is preferable to use a polyol having a polypropylene skeleton as the polyol component to be reacted with the polyisocyanate, since the polyisocyanate (A1) has a low viscosity and is easy to handle at low temperatures.
- the polyol component to be reacted with the polyisocyanate has a number average molecular weight (Mn) of 300 to 5,000, more preferably 350 to 3,000.
- Ether polyols are preferably used.
- the proportion of polyether polyol having a number average molecular weight (Mn) of 300 to 5,000 in the polyol component is preferably 50% by mass or more.
- the total polyol component may be a polyether polyol having a number average molecular weight (Mn) of 300-5,000.
- the weight average molecular weight (Mw) and number average molecular weight (Mn) are values measured by gel permeation chromatography (GPC) under the following conditions.
- Measuring device HLC-8320GPC manufactured by Tosoh Corporation Column; TSKgel 4000HXL, TSKgel 3000HXL, TSKgel 2000HXL, TSKgel 1000HXL manufactured by Tosoh Corporation Detector; RI (differential refractometer) Data processing; Multi-station GPC-8020modelII manufactured by Tosoh Corporation Measurement conditions; column temperature 40°C Solvent; tetrahydrofuran flow rate; 0.35 ml/min standard; monodisperse polystyrene sample; 0.2% by mass of tetrahydrofuran solution in terms of resin solid content filtered through a microfilter (100 ⁇ l)
- the polyisocyanate to be reacted with the polyol component preferably contains an aromatic polyisocyanate because of its excellent reactivity with the polyamine (C) described later.
- the amount of the aromatic polyisocyanate to be blended is preferably 30 parts by mass or more, more preferably 40 parts by mass or more, for 100 parts by mass of the total charged amount for synthesizing the polyisocyanate (A1).
- the upper limit of the amount of the aromatic polyisocyanate compounded is preferably 60 parts by mass or less, more preferably 55 parts by mass or less.
- polyisocyanate to be reacted with the polyol component, it is preferable to use at least one of aliphatic polyisocyanate and aliphatic polyisocyanate derivative together with aromatic polyisocyanate from the viewpoint of storage stability.
- the reaction ratio of the polyisocyanate and the polyol component in the polyisocyanate (A1) is such that the equivalent ratio [isocyanate group/hydroxyl group] between the isocyanate group in the polyisocyanate and the hydroxyl group in the polyol component is 1.5 to 5.0. A range is preferred.
- the polyisocyanate (A) employing such a polyisocyanate (A1) has an appropriate viscosity of the polyisocyanate composition (X) containing it, and the coating property is improved, and the polyisocyanate (A ) is preferable because the cohesive force of the coating film made of the two-component curing adhesive containing is improved.
- the polyisocyanate (A) preferably has a weight average molecular weight (Mw) in the range of 100 to 10,000 from the viewpoint of shortening the aging time and ensuring proper packaging properties. A range is more preferred.
- Mw weight average molecular weight
- the polyisocyanate (A) is the polyisocyanate (A1), it preferably has a weight average molecular weight (Mw) in the range of 300 to 10,000.
- the polyisocyanate (A) preferably has an isocyanate content of 5 to 20% by mass.
- the polyisocyanate composition (X) containing such a polyisocyanate (A) is preferable because it has an appropriate resin viscosity and is excellent in coatability.
- the isocyanate content of polyisocyanate (A) is a value determined by a titration method using di-n-butylamine.
- polyol (B) examples include ethylene glycol, propylene glycol, 1,3-propanediol, 1,4-butanediol, 1,5-pentanediol, 3-methyl-1,5-pentanediol, 1,6 - hexanediol, neopentyl glycol, methylpentanediol, dimethylbutanediol, butylethylpropanediol, diethylene glycol, triethylene glycol, tetraethylene glycol, dipropylene glycol, tripropylene glycol, bishydroxyethoxybenzene, 1,4-cyclohexanediol , 1,4-cyclohexanedimethanol, glycols such as triethylene glycol;
- trifunctional or tetrafunctional aliphatic alcohols such as glycerin, trimethylolpropane, and pentaerythritol; bisphenols such as bisphenol A, bisphenol F, hydrogenated bisphenol A, and hydrogenated bisphenol F; dimer diols;
- polyester polyol (2) obtained by reacting a bifunctional polyol such as the glycol, dimer diol, or bisphenol with a polyvalent carboxylic acid
- polyester polyol (3) obtained by reacting the trifunctional or tetrafunctional aliphatic alcohol with a polycarboxylic acid
- a polyester polyol (4) obtained by reacting a bifunctional polyol, the trifunctional or tetrafunctional aliphatic alcohol, and a polyvalent carboxylic acid
- Polyester polyol (5) which is a polymer of hydroxy acids such as dimethylolpropionic acid and castor oil fatty acid
- Polyester polyether polyols obtained by reacting the polyester polyols (1) to (5), the polyether polyols, and an aromatic or aliphatic polyisocyanate
- polyester polyurethane polyols obtained by polymerizing the polyester polyols (1) to (5) with aromatic or aliphatic polyisocyanates
- Castor oil dehydrated castor oil, hydrogenated castor oil,
- Examples of the polyvalent carboxylic acid used for producing the polyester polyol (2), (3) or (4) include succinic acid, adipic acid, azelaic acid, sebacic acid, dodecanedicarboxylic acid, maleic anhydride, and fumaric acid.
- a tertiary amine compound having a plurality of hydroxyl groups may be used as the polyol (B).
- a tertiary amine compound having a plurality of hydroxyl groups not only cures when the hydroxyl groups react with the polyisocyanate (A), but also functions as a curing accelerator because the amine structure accelerates the curing reaction.
- the number of hydroxyl groups is 2 or more, preferably 2 to 6.
- a tertiary amine compound having a plurality of hydroxyl groups may have one or more tertiary amino groups, preferably one or two.
- tertiary amine compounds having a plurality of hydroxyl groups include polypropylene glycol ethylene diamine ether, tri(1,2-polypropylene glycol) amine, N-ethyldiethanolamine, N-methyl-N-hydroxyethyl-N-hydroxy ethoxyethylamine, pentakishydroxypropyldiethylenetriamine, tetrakishydroxypropylethylenediamine, N,N,N',N'-tetrakis(2-hydroxypropyl)ethylenediamine, triethanolamine, triethanolamine propoxylated and the like.
- a commercially available product may be used as the tertiary amine compound having multiple hydroxyl groups.
- Examples of commercially available products include EDP-300 manufactured by ADEKA Corporation, ED-500 and TE-360 manufactured by Kokuto Kako, and VORANOL TM800 Polyol manufactured by DOW.
- the mixing ratio of the polyol other than the tertiary amine compound in the polyol (B) and the tertiary amine compound (polyol other than the tertiary amine compound/ The tertiary amine compound (mass ratio)) is preferably from 100/5 to 100/70, more preferably from 100/10 to 100/70.
- Polyol (B) preferably contains a polyol having a polyether skeleton, and more preferably contains a polyol having a polypropylene skeleton.
- a polyol (B) has a viscosity that enables coating at a temperature of 25° C. to 60° C. even if it is a non-solvent type.
- the two-component curing adhesive containing such a polyol (B) is preferable because it exhibits excellent adhesion strength to metal oxides such as silica and/or alumina, metals such as aluminum, and resin films.
- the content of the polyol having a polyether skeleton is preferably 5% by mass or more, more preferably 10% by mass or more, more preferably 15% by mass, based on the total amount of the polyol (B) from the viewpoint of coatability. It is more preferable to be above.
- the upper limit of the content of the polyol having a polyether skeleton is not particularly limited, and the total amount of the polyol (B) may be a polyol having a polyether skeleton. From the viewpoint, it is preferably 95% by mass or less.
- Polyol (B) is castor oil, dehydrated castor oil, hydrogenated castor oil that is a hydrogenated product of castor oil, and 5 to 50 moles of alkylene oxide added to castor oil, from the viewpoint of the initial cohesive strength and coatability of the two-component curing adhesive. It preferably contains at least one castor oil-based compound selected from the group consisting of castor oil-based polyols such as castor oil-based polyols. These castor oil-based compounds are preferably 5% by mass or more, more preferably 10% by mass or more, more preferably 15% by mass or more, and 20% by mass of the total amount of polyol (B). It is more preferable to be above. Also, the upper limit of the castor oil-based compound is not particularly limited, and the total amount of the polyol (B) may be a castor oil-based compound, but from the viewpoint of coatability, it is preferably 95% by mass or less.
- the polyol (B) may contain a highly reactive low-molecular-weight polyol (liquid at room temperature and having a molecular weight of about 150 or less). By containing such a low-molecular-weight polyol, the reaction with the polyisocyanate (A) can be accelerated. On the other hand, if the amount of the low-molecular-weight polyol is too large, the reaction with the polyisocyanate (A) may be too fast. Therefore, the content of the low-molecular-weight polyol is preferably 5% by mass or less, more preferably 3% by mass or less, of the polyol (B).
- the viscosity of the polyol (B) is 400 to 5000, so the coatability is improved, and the cohesive force of the two-component curing adhesive is improved, which is preferable. .
- the hydroxyl value of the polyol (B) is preferably 50 mgKOH/g or more and 300 mgKOH/g or less, more preferably 100 mgKOH/g or more and 250 mgKOH/g or less.
- the hydroxyl value of the polyol (B) can be measured by the hydroxyl value measuring method described in JIS-K0070.
- the polyol composition (Y) preferably contains a polyamine (C).
- Polyamine (C) functions as a curing accelerator.
- the polyamine (C) known ones can be used without particular limitation.
- Polyamine (C) has two amino groups ( NH2 group, NHR group (R represents an alkyl group)) in the molecule in order to maintain the toughness of the coating film made of a two-component curing adhesive. It is desirable that the compound has the above.
- polyamine (C) examples include methylenediamine, ethylenediamine, isophoronediamine, 3,9-dipropanamine-2,4,8,10-tetraoxapyrodundecane, lysine, phenylenediamine, 2,2,4- trimethylhexamethylenediamine, tolylenediamine, hydrazine, piperazine, hexamethylenediamine, propylenediamine, dicyclohexylmethane-4,4-diamine, 2-hydroxyethylethylenediamine, di-2-hydroxyethylethylenediamine, di-2-hydroxyethylpropylene diamine, 2-hydroxypropylethylenediamine, or di-2-hydroxypropylethylenediamine, poly(propylene glycol) diamine, poly(propylene glycol) triamine, poly(propylene glycol) tetraamine, 1,2-diaminopropane, 1,3-diamino propane,
- 1,4-diaminobutane 1,5-diaminopentane, 1,6-diaminohexane, 1,7-diaminoheptane, 1,8-diaminooctane, 1,9-diaminononane, 1,10-diaminodecane, etc.
- benzyl amine diethylenetriamine, dipropylenetriamine, triethylenetetramine, tripropylenetetramine, tetraethylenepentamine, tetrapropylenepentamine, pentaethylenehexamine, nonaethylenedecamine, trimethylhexamethylenediamine, etc., tetra(aminomethyl)methane, tetrakis ( 2-aminoethylaminomethyl)methane, 1,3-bis(2′-aminoethylamino)propane, triethylene-bis(trimethylene)hexamine, bis(3-aminoethy
- polyamine (C) it is preferable to use a polyetheramine having a polyether structure in the main chain in order to maintain the flexibility of the coating film composed of the two-component curing adhesive.
- These polyamines (C) may be used alone or in combination of two or more.
- a commercially available product may be used as the polyamine (C).
- Commercially available products include EC-310 and EC-303 manufactured by BASF.
- the functional group in the polyisocyanate composition (X) (the isocyanate group of the polyisocyanate (A)) and the functional group in the polyol composition (Y) (the hydroxyl group of the polyol (B), the amino group of the polyamine (C), group) molar ratio [isocyanate group / (hydroxyl group + amino group)] is preferably 0.5 to 5.0, and from the viewpoint of the adhesive performance of the two-component curing adhesive, 1.0 to 3.0 is more desirable.
- the ratio of the polyol (B) and the polyamine (C) in the polyol composition (Y) is such that the molar ratio [amino group/hydroxyl group] of the amino group derived from the polyamine (C) and the hydroxyl group derived from the polyol (B) is 0. .001 to 2.0 is desirable, and from the viewpoint of achieving both the adhesive strength of the two-part curing adhesive, the processed appearance, and the practicality of workability, the range of 0.1 to 1.0 is more preferable. preferable.
- the above molar ratio is 0.001 or more, the workability of the laminated film produced using the two-component curing adhesive becomes favorable.
- the molar ratio is 2.0 or less, the adhesion strength of the two-component curing adhesive becomes favorable.
- the two-component curable adhesive of the present embodiment can be used as a solventless adhesive, but the two-component curable adhesive of the present embodiment may contain a solvent if necessary.
- the "solvent” refers to a highly soluble organic solvent capable of dissolving the polyisocyanate composition (X) and/or the polyol composition (Y).
- solvent-free refers to not containing these highly soluble organic solvents.
- solvents include toluene, xylene, methylene chloride, tetrahydrofuran, methanol, ethanol, isopropyl alcohol, methyl acetate, ethyl acetate, n-butyl acetate, acetone, and methyl ethyl ketone (MEK). , cyclohexanone, n-hexane, cyclohexane, and the like.
- solvents include toluene, xylene, methylene chloride, tetrahydrofuran, methyl acetate, and ethyl acetate are particularly highly soluble organic solvents.
- the two-component curable adhesive of this embodiment can be used by diluting it with a solvent so as to obtain the desired viscosity when it is required to lower the viscosity.
- a solvent may be used to dilute either one of the polyisocyanate composition (X) or the polyol composition (Y), or both.
- organic solvents examples include methanol, ethanol, isopropyl alcohol, methyl acetate, ethyl acetate, n-butyl acetate, acetone, methyl ethyl ketone (MEK), cyclohexanone, Examples include toluene, xylene, n-hexane, cyclohexane and the like.
- ethyl acetate and/or methyl ethyl ketone (MEK) it is preferable to use ethyl acetate, from the viewpoint of the solubility of the polyisocyanate composition (X) and the polyol composition (Y).
- MEK methyl ethyl ketone
- the content of the organic solvent in the two-component curing adhesive of the present embodiment can be appropriately determined according to the required viscosity, and can be, for example, 20 to 50% by mass.
- the two-component curing adhesive of this embodiment may contain a catalyst.
- the catalyst may be contained in either one of the polyisocyanate composition (X) and the polyol composition (Y), or may be contained in both.
- the catalyst generally has a high reactivity with the polyisocyanate composition, and after the polyisocyanate composition (X) and the polyol composition (Y) are brought into contact with each other, the catalyst is effectively activated. It is preferably contained only in (Y).
- the catalyst may be contained in the polyisocyanate composition (X) and/or the polyol composition (Y) during coating of the two-component curing adhesive.
- the two-component curing adhesive contains a catalyst
- the curing of the two-component curing adhesive is accelerated, and the laminate film produced using the two-component curing adhesive is exposed to harmful low-grade compounds such as aromatic amines. Elution of molecular chemicals can be suppressed. That is, the catalyst also works as a curing accelerator like polyamine (C) and the like.
- the catalyst is not particularly limited as long as it promotes the urethanization reaction between the polyisocyanate composition (X) and the polyol composition (Y).
- catalysts that can be used include metal-based catalysts, amine-based catalysts, diazabicycloundecene (DBU), aliphatic cyclic amide compounds, and titanium chelate complexes.
- Metal-based catalysts include metal complex-based catalysts, inorganic metal-based catalysts, and organic metal-based catalysts.
- the metal complex catalyst from the group consisting of Fe (iron), Mn (manganese), Cu (copper), Zr (zirconium), Th (thorium), Ti (titanium), Al (aluminum) and Co (cobalt) Acetylacetonate salts of selected metals and the like are included. Specific examples include iron acetylacetonate, manganese acetylacetonate, copper acetylacetonate, and zirconia acetylacetonate.
- iron acetylacetonate Fe(acac) 3
- manganese acetylacetonate Mn(acac) 2
- Organometallic catalysts include stannus diacetate, stannus dioctoate, stannus dioleate, stannus dilaurate, dibutyltin oxide, dibutyltin diacetate, dibutyltin dilaurate, dibutyltin dichloride, dioctyltin dilaurate, nickel octylate, nickel naphthenate, cobalt octylate, cobalt naphthenate, bismuth octylate, bismuth naphthenate, bismuth neodecanoate, zinc neodecanoate and the like.
- preferred organometallic catalysts are stannous dioctoate, dibutyltin dilaurate, bismuth neodecanoate, zinc neodecanoate, or mixtures thereof.
- amine-based catalysts examples include triethylenediamine, 2-methyltriethylenediamine, quinuclidine, and 2-methylquinuclidine.
- triethylenediamine and/or 2-methyltriethylenediamine are preferably used as the amine-based catalyst because of their excellent catalytic activity and industrial availability.
- tertiary amine catalysts include N,N,N',N'-tetramethylethylenediamine, N,N,N',N'-tetramethylpropylenediamine, N,N,N',N'',N ′′-pentamethyldiethylenetriamine, N,N,N′,N′′,N′′-pentamethyl-(3-aminopropyl)ethylenediamine, N,N,N′,N′′,N′′-pentamethyldipropylenetriamine, N, N,N',N'-tetramethylhexamethylenediamine, bis(2-dimethylaminoethyl)ether, dimethylethanolamine, dimethylisopropanolamine, dimethylaminoethoxyethanol, N,N-dimethyl-N'-(2-hydroxy ethyl)ethylenediamine, N,N-dimethyl-N'-(2-hydroxyethyl)propanediamine, bis(dimethylaminoprop
- aliphatic cyclic amide compounds used as catalysts include ⁇ -valerolactam, ⁇ -caprolactam, ⁇ -enanthrolactam, ⁇ -capryllactam and ⁇ -propiolactam.
- ⁇ -caprolactam can more effectively accelerate the curing of two-component curing adhesives.
- the content of the catalyst in the two-component curing adhesive of this embodiment is not particularly limited, and can be a known amount.
- the content of the catalyst can be, for example, 0.001 to 5.0% by mass with respect to the total solid content of the two-component curing adhesive.
- the two-component curing adhesive of this embodiment may contain an adhesion promoter.
- the adhesion promoter may be contained in either one of the polyisocyanate composition (X) and the polyol composition (Y), or may be contained in both. Since the adhesion promoter has high reactivity with the polyisocyanate composition (X), it is preferred to act after the polyisocyanate composition (X) and the polyol composition (Y) are brought into contact with each other. Therefore, the adhesion promoter is preferably contained only in the polyol composition (Y).
- the adhesion promoter may be contained in the polyisocyanate composition (X) and/or the polyol composition (Y) during coating of the two-component curing adhesive. Examples of adhesion promoters include silane coupling agents, titanate-based coupling agents, aluminum-based coupling agents, epoxy resins, and the like.
- Silane coupling agents include, for example, ⁇ -aminopropyltriethoxysilane, 3-glycidyloxypropyltrimethoxysilane, ⁇ -aminopropyltrimethoxysilane, N- ⁇ (aminoethyl)- ⁇ -aminopropyltrimethoxysilane, Aminosilanes such as N- ⁇ (aminoethyl)- ⁇ -aminopropyltrimethyldimethoxysilane, N-phenyl- ⁇ -aminopropyltrimethoxysilane; ⁇ -(3,4-epoxycyclohexyl)ethyltrimethoxysilane, ⁇ -glycides epoxysilanes such as xypropyltrimethoxysilane and ⁇ -glycidoxypropyltriethoxysilane; vinylsilanes such as vinyltris( ⁇ -methoxyethoxy)silane, vinyltrie
- Titanate-based coupling agents include, for example, tetraisopropoxytitanium, tetra-n-butoxytitanium, butyl titanate dimer, tetrastearyl titanate, titanium acetylacetonate, titanium lactate, tetraoctylene glycol titanate, titanium lactate, tetrastearoxy Titanium etc. can be mentioned.
- aluminum-based coupling agents include acetoalkoxyaluminum diisopropylate.
- epoxy resin generally commercially available epi-bis type, novolac type, ⁇ -methyl epichloro type, cyclic oxirane type, glycidyl ether type, glycidyl ester type, polyglycol ether type, glycol ether type, epoxidized fatty acid ester type, polyvalent carboxylic acid ester type, aminoglycidyl type, resorcinol type, and other epoxy resins.
- the content of the adhesion promoter in the two-component curing adhesive of this embodiment is not particularly limited, and can be a known amount.
- the content of the adhesion promoter can be, for example, 0 to 50% by mass with respect to the total solid content of the two-component curing adhesive.
- the two-component curing adhesive of the present embodiment may be used in combination with a pigment, if necessary.
- the pigment may be contained in either one of the polyisocyanate composition (X) and the polyol composition (Y), or may be contained in both.
- the pigment may be contained in the polyisocyanate composition (X) and/or the polyol composition (Y) during coating of the two-component curing adhesive.
- the pigment is not particularly limited, and includes various pigments.
- pigments include extender pigments, white pigments, black pigments, gray pigments, red pigments, brown pigments, green pigments, blue pigments, and metal powders described in the 1970 edition of Handbook of Paint Materials (edited by the Japan Paint Manufacturers Association).
- organic pigments such as pigments, luminescent pigments and pearlescent pigments, inorganic pigments, and plastic pigments.
- organic pigments examples include various insoluble azo pigments such as Benzidine Yellow, Hansa Yellow and Laked 4R; soluble azo pigments such as Laked C, Carmine 6B and Bordeaux 10; various (copper) phthalocyanine pigments such as phthalocyanine blue and phthalocyanine green.
- insoluble azo pigments such as Benzidine Yellow, Hansa Yellow and Laked 4R
- soluble azo pigments such as Laked C, Carmine 6B and Bordeaux 10
- various (copper) phthalocyanine pigments such as phthalocyanine blue and phthalocyanine green.
- Pigments various chlorine dyeing lakes such as rhodamine lake and methyl violet lake; various mordant pigments such as quinoline lake and fast sky blue; various vat dyes such as anthraquinone pigments, thioindigo pigments and perinone pigments dye-based pigments; various quinacridone-based pigments such as Cincasia Red B; various dioxazine-based pigments such as dioxazine violet; various condensed azo pigments such as chromophtal;
- inorganic pigments include various chromates such as yellow lead, zinc chromate, and molybdate orange; various ferrocyanic compounds such as Prussian blue; titanium oxide, zinc white, mapico yellow, iron oxide, red iron oxide, and chromium oxide.
- various metal oxides such as green and zirconium oxide; various sulfides and selenides such as cadmium yellow, cadmium red, and mercury sulfide; various sulfates such as barium sulfate and lead sulfate; various types such as calcium silicate and ultramarine blue various carbonates such as calcium carbonate and magnesium carbonate; various phosphates such as cobalt violet and manganese purple; various metal powders such as aluminum powder, gold powder, silver powder, copper powder, bronze powder and brass powder. pigments; flake pigments of these metals, mica flake pigments; metallic pigments and pearl pigments such as mica flake pigments coated with metal oxides and mica-like iron oxide pigments; graphite, carbon black and the like.
- Extender pigments include, for example, precipitated barium sulfate, rice flour, precipitated calcium carbonate, calcium bicarbonate, Kansui stone, alumina white, silica, hydrous fine silica (white carbon), ultrafine anhydrous silica (Aerosil), silica sand (silica sand), talc, precipitated magnesium carbonate, bentonite, clay, kaolin, loess, and the like.
- plastic pigments include "Glandole PP-1000" and "PP-2000S” manufactured by DIC Corporation.
- inorganic oxides such as titanium oxide and zinc oxide as white pigments, and carbon black as black pigments, since they are excellent in durability, weather resistance, and design.
- the content of the pigment in the two-component curing adhesive of the present embodiment is 1 to 400 parts by mass with respect to 100 parts by mass of the total solid content of the polyisocyanate composition (X) and the polyol composition (Y). is preferred, and 10 to 300 parts by mass is more preferred.
- the content of the pigment is 1 to 400 parts by mass, a two-part curing adhesive having excellent adhesion and anti-blocking properties can be obtained.
- the two-component curing adhesive of the present invention may contain other additives in addition to the components described above, if necessary.
- the additive may be contained in either one of the polyisocyanate composition (X) and the polyol composition (Y), or may be contained in both.
- the additive may be contained in the polyisocyanate composition (X) and/or the polyol composition (Y) during coating of the two-component curing adhesive.
- Additives include, for example, leveling agents; inorganic fine particles such as colloidal silica and alumina sol; polymethylmethacrylate-based organic fine particles; antifoaming agents; Deactivator; peroxide decomposer; flame retardant; reinforcing agent; plasticizer; lubricant; rust inhibitor; fluorescent whitening agent; is mentioned.
- the two-component curable adhesive of the present embodiment is a two-component curable adhesive using a curing reaction between the polyisocyanate composition (X) and the polyol composition (Y), wherein the polyisocyanate composition (X) is It contains polyisocyanate (A), polyol composition (Y) contains polyol (B), and extensional viscosity of polyisocyanate composition (X) and polyol composition (Y) is 0.1 to 10 Pa ⁇ s.
- the two-component curing adhesive of the present embodiment can be used in the case of producing a laminated film by a production method having a two-component separate application step, the polyisocyanate composition (X) applied on the first film, In the step of contacting the polyol composition (Y) coated on the second film, misting is less likely to occur, and the initial cohesion is also excellent.
- the two-component curable adhesive of the present embodiment can be used, for example, when manufacturing a laminated film using a manufacturing method including a two-component mixed coating process and a manufacturing method including a two-component separate coating process. It can be suitably used for
- the two-component curing adhesive of the present embodiment is 0.1 to 10 Pa s, thereby suppressing the occurrence of misting. can.
- the initial cohesive force may be insufficient, but the extensional viscosity of the polyisocyanate composition (X) and the polyol composition (Y) is 0.1 to 10 Pa s. This makes it possible to solve the problem of initial cohesion. For this reason, the two-component curing adhesive of the present embodiment can be used particularly suitably when manufacturing a laminated film using a method having a two-component separate coating process.
- the elongational viscosity of the polyisocyanate composition (X) and the polyol composition (Y) is 0.1 to 10 Pa ⁇ s.
- the two-component curing adhesive of the present embodiment has good reactivity between the polyol composition (Y) and the polyisocyanate composition (X). Therefore, the aging temperature can be lowered and the aging time can be shortened.
- FIG. 1 is a cross-sectional view showing an example of the laminated film according to this embodiment.
- the laminated film 11a of this embodiment has an adhesive layer 10 between the first film W1 and the second film W2.
- the adhesive layer 10 is made of the cured two-component curing adhesive of the above embodiment.
- the film In the laminated film 11a of the present embodiment, it is preferable to use plastic films used for known laminated films for the films used as the first film W1 and the second film W2.
- the first film W1 include base films such as polyethylene terephthalate (hereinafter sometimes abbreviated as "PET") film, nylon (OPA) film, biaxially oriented polypropylene (OPP) film, various vapor deposition films, Aluminum foil or the like can be used.
- PET polyethylene terephthalate
- OPA nylon
- OPP biaxially oriented polypropylene
- various vapor deposition films Aluminum foil or the like
- Aluminum foil or the like can be used.
- a sealant film such as an unstretched polypropylene (CPP) film or a linear low density polyethylene (LLDPE) film can be used.
- CPP unstretched polypropylene
- LLDPE linear low density polyethylene
- Paper such as natural paper, synthetic paper, and coated paper may be used as the first film W1 and the second film W2.
- a printed layer may be provided on the outer surface or inner surface side of the first film W1 and/or the second film W2, if necessary.
- the laminated film 11a of the present embodiment is industrially used as a flexible packaging film, a flexible packaging (package whose shape is formed by putting contents in it) material, a packaging material for filling detergents, medicines, foods, beverages, etc. can be used as intended.
- Specific examples of detergents and chemicals include liquid laundry detergents, liquid kitchen detergents, liquid bath detergents, liquid bath soaps, liquid shampoos, and liquid conditioners. Foods and beverages are not particularly limited.
- the laminated film 11a of this embodiment can be used as a package by forming it into a bag shape.
- the laminated film 11a of the present embodiment has an adhesive layer 10 between the first film W1 and the second film W2, and the adhesive layer 10 is formed from the cured two-component curable adhesive of the above embodiment.
- the laminated film 11a of the present embodiment can be manufactured using the two-component curable adhesive of the above embodiment, which has excellent initial cohesive strength and is less prone to misting even when the step of applying it onto the film is performed. . Therefore, the laminated film of the present embodiment can be efficiently manufactured using a manufacturing method such as a manufacturing method including a two-component mixed coating process and a manufacturing method including a two-component separate coating process.
- the two-component curing adhesive of the above embodiment cures in a short time and/or at a low temperature, the laminated film 11a of this embodiment can be produced with a small amount of energy.
- FIG. 2 is a front view of the laminated film manufacturing apparatus according to the present embodiment.
- 3 is a front view showing a main part of a polyisocyanate coating section in the laminated film manufacturing apparatus shown in FIG. 2.
- FIG. 4 is a front view showing a main part of a polyol coating section in the laminated film manufacturing apparatus shown in FIG. 2.
- the laminated film manufacturing apparatus 1 shown in FIG. 2 uses the two-component curing adhesive of the present embodiment described above to separate the first film W1 unwound from the roll and the second film W2 unwound from the roll.
- This apparatus forms the adhesive layer 10 between the first film W1 and the second film W2 by sticking them together, and manufactures the above-described laminated film 11a of the present embodiment wound into a roll.
- the laminated film manufacturing apparatus 1 of the present embodiment includes a first unwinding section 11, a polyisocyanate coating section 12 (first coating section), a second unwinding section 13, A polyol coating unit 14 (second coating unit) and a bonding device 15 are provided.
- the first unwinding section 11 delivers the first film W1 to the polyisocyanate coating section 12 .
- the first film W1 is rotatably mounted on the film mounting portion 111 of the first unwinding portion 11 .
- the polyisocyanate coating section 12 applies the polyisocyanate composition (X) of the two-component curing adhesive of the present embodiment to the first film W1 delivered from the first unwinding section 11 .
- the polyisocyanate coating section 12 is a four-roll squeeze roll coater.
- the polyisocyanate coating section 12 includes an application roll 121 , a doctor roll 122 , a metering roll 123 , a coating roll 124 and a backing roll 125 .
- a liquid reservoir 120 is provided at a portion where the application roll 121 and the doctor roll 122 face each other.
- the application roll 121 is a roll having an outer peripheral surface made of an elastic material such as rubber.
- the doctor roll 122 is a roll having an outer peripheral surface made of metal (inelastic material). As shown in FIG. 3, the application roll 121 and the doctor roll 122 are rotatably supported by the polyisocyanate coating section 12 so that their rotation axes are parallel to each other. The outer peripheral surface of the application roll 121 and the outer peripheral surface of the doctor roll 122 face each other with a minute gap therebetween.
- a pair of barrier plates 126 is installed at a predetermined interval in the direction of the rotation axis of the application roll 121 and the doctor roll 122 above the portion where the application roll 121 and the doctor roll 122 face each other.
- a liquid reservoir 120 is formed by the pair of barrier plates 126 , the outer peripheral surface of the application roll 121 , and the outer peripheral surface of the doctor roll 122 .
- the liquid reservoir 120 temporarily stores the polyisocyanate composition (X).
- the polyisocyanate composition (X) is supplied to the liquid reservoir 120 from a polyisocyanate supply section (not shown). Thereby, the polyisocyanate composition (X) stored in the liquid reservoir 120 is held at a constant amount.
- the doctor roll 122 preferably has a temperature control section (not shown).
- the temperature control section keeps the polyisocyanate composition (X) stored in the liquid reservoir section 120 at a constant temperature and stabilizes the viscosity of the polyisocyanate composition (X). Thereby, the outer peripheral surface of the doctor roll 122 is kept at a constant temperature.
- the application roll 121 and doctor roll 122 rotate downward in the liquid reservoir 120 .
- the outer peripheral surface of the doctor roll 122 is coated with the polyisocyanate composition (X) that has passed through the minute gaps.
- the polyisocyanate coating section 12 rotatably supports a metering roll 123, a coating roll 124, and a backing roll 125.
- the polyisocyanate composition (X) applied to the outer peripheral surface of the doctor roll 122 is transferred to the metering roll 123 .
- the rotating shaft of the metering roll 123 is arranged parallel to the rotating shaft of the doctor roll 122 .
- the outer peripheral surface of the metering roll 123 is made of an elastic material such as rubber. The outer peripheral surface of the metering roll 123 is pressed against the outer peripheral surface of the doctor roll 122 .
- the polyisocyanate composition (X) applied to the outer peripheral surface of the metering roll 123 is transferred to the coating roll 124 .
- the rotation axis of the coating roll 124 is arranged parallel to the rotation axis of the metering roll 123 .
- the outer peripheral surface of the coating roll 124 is formed of a metal material. The outer peripheral surface of the coating roll 124 is pressed against the outer peripheral surface of the metering roll 123 .
- the backing roll 125 is arranged so that the rotating shafts of the coating roll 124 are parallel to each other.
- the backing roll 125 sandwiches the second film W2 between itself and the coating roll 124, and conveys the second film W2.
- the backing roll 125 assists the transfer of the polyisocyanate composition (X) applied to the outer peripheral surface of the coating roll 124 to the first film W1.
- the outer peripheral surface of the backing roll 125 is made of an elastic material such as rubber.
- the coating roll 124 preferably has a constant temperature of the outer peripheral surface by a temperature control unit (not shown). This stabilizes the viscosity of the polyisocyanate composition (X) applied to the first film W1.
- misting occurs when the polyisocyanate composition (X) moves between rolls due to transfer. Locations where misting usually occurs include, for example, the area where the doctor roll 122 and the metering roll 123 are in pressure contact, the area where the metering roll 123 and the coating roll 124 are in pressure contact, and the coating roll 124 and the backing roll. The vicinity where 125 is press-contacted can be mentioned.
- misting it is necessary to reduce the rotation speed of each roll and the transport speed of the first film W1 in order to suppress the occurrence of misting.
- the conveying speed of the first film W1 is lowered, the production efficiency of the laminated film 11a is lowered.
- misting can be suppressed by using a composition having a specific elongational viscosity as the polyisocyanate composition (X).
- a composition having a specific elongational viscosity as the polyisocyanate composition (X).
- the laminated film 11a having excellent properties can be efficiently produced.
- the polyisocyanate composition (X) is applied using a roll coater as in this embodiment, there are many locations where misting may occur. Therefore, the effect of strictly controlling the elongational viscosity of the polyisocyanate composition (X) becomes more pronounced.
- the second unwinding section 13 delivers the second film W2 to the polyol coating section 14 .
- the second film W2 is rotatably mounted on the film mounting portion 131 of the second unwinding portion 13 .
- the polyol coating section 14 applies the polyol composition (Y) of the two-component curing adhesive of the present embodiment to the second film W2 delivered from the second unwinding section 13 .
- the polyol coating unit 14, as shown in FIG. 4, is a gravure coating machine (gravure coater) that applies the polyol composition (Y) by gravure printing.
- the polyol coating section 14 includes a gravure roll 141 , a chamber 142 , an impression cylinder 143 , a coating liquid tank 144 , a pump 145 and a temperature controller 146 .
- the gravure roll 141 is a metal roll rotatably supported by the polyol coating section 14 .
- a plurality of recesses are formed on the surface of the gravure roll 141 by, for example, laser engraving. By changing the volume, opening ratio, depth, etc. of the recesses, the amount of the coating liquid applied to the surface of the gravure roll 141 can be adjusted.
- the gravure pattern applied to the surface of the gravure roll 141 is not particularly limited, and may be, for example, a honeycomb pattern.
- the chamber 142 is a container that stores the polyol composition (Y).
- the chamber 142 is arranged on one radial side of the gravure roll 141 .
- the chamber 142 has a storage part 142a that stores the polyol composition (Y).
- the storage part 142a is open to the gravure roll 141 side. A part of the outer peripheral surface of the gravure roll 141 is immersed in the polyol composition (Y) stored in the storage part 142a.
- the reservoir 142a is sealed by a doctor blade 142b, a seal plate 142c and a pair of side plates 142d.
- the chamber 142 has a plate-like doctor blade 142b.
- the doctor blade 142b protrudes toward the gravure roll 141 from the upper end of the opening of the reservoir 142a.
- the material of the doctor blade 142b is not particularly limited, and may be metal or resin, for example, stainless steel.
- the tip of the doctor blade 142 b is pressed against the outer peripheral surface of the gravure roll 141 .
- the tip of the doctor blade 142b seals the downstream side of the reservoir 142a in the roll rotation direction.
- the doctor blade 142b scrapes off excess polyol composition (Y) adhering to the outer peripheral surface of the gravure roll 141 by rotating the gravure roll 141 and weighs it.
- the chamber 142 has a plate-like seal plate 142c.
- the seal plate 142c is made of resin.
- the seal plate 142c protrudes toward the gravure roll 141 from the lower end of the opening of the reservoir 142a.
- the tip of the seal plate 142 c is pressed against the outer peripheral surface of the gravure roll 141 .
- the tip of the seal plate 142c seals the upstream side of the reservoir 142a in the roll rotation direction.
- the chamber 142 has a side plate 142d made of resin.
- the side plates 142d are attached to both side surfaces of the chamber 142, that is, both ends of the gravure roll 141 in the rotation axis direction.
- the side surface of the side plate 142 d on the side of the gravure roll 141 has an arc shape along the shape of the gravure roll 141 and is pressed against the gravure roll 141 .
- the impression cylinder 143 holds the second film W2 between itself and the gravure roll 141, and conveys the second film W2.
- the impression cylinder 143 presses the second film W2 against the gravure roll 141 to transfer the polyol composition (Y) applied to the outer peripheral surface of the gravure roll 141 to the second film W2.
- misting occurs when the polyol composition (Y) moves between rolls due to transfer.
- the misting of the polyol composition (Y) occurs in the vicinity of the pressure contact between the gravure roll 141 and the impression cylinder 143 . If misting occurs, it is necessary to reduce the rotation speed of each roll and the conveying speed of the second film W2 in order to suppress the occurrence of misting.
- the conveying speed of the second film W2 is lowered, the production efficiency of the laminated film 11a is lowered.
- the polyol composition (Y) by using a composition having a specific elongational viscosity as the polyol composition (Y), the occurrence of misting can be suppressed. As a result, the laminated film 11a having excellent properties can be efficiently manufactured.
- the coating liquid tank 144 is a container that stores the polyol composition (Y). As shown in FIG. 4, the coating liquid tank 144 is connected via a pipe to a pump 145 for flowing the polyol composition (Y) into the chamber 142 . Also, the coating liquid tank 144 is connected to the chamber 142 via a pipe. As a result, the polyol composition (Y) overflowing from the reservoir 142 a of the chamber 142 is recovered in the coating liquid tank 144 .
- the pump 145 is connected to the coating liquid tank 144 and the chamber 142 via piping.
- the pump 145 supplies the polyol composition (Y) stored in the coating liquid tank 144 to the reservoir 142 a of the chamber 142 .
- a sine pump for example, can be used as the pump 145 .
- the temperature controller 146 adjusts the temperature of the polyol composition (Y) stored in the coating liquid tank 144. This keeps the temperature of the polyol composition (Y) constant and stabilizes the viscosity of the polyol composition (Y).
- the temperature controller 146 is, for example, a water temperature controller that heats water, which is a heat medium, with a heater and circulates around the polyol composition (Y) stored in the coating liquid tank 144 .
- the bonding device 15 includes a bonding section 151 and a winding section 152, as shown in FIG.
- the bonding portion 151 is a surface coated with the polyisocyanate composition (X) in the first film W1 delivered from the polyisocyanate coating portion 12 and a polyol composition in the second film W2 delivered from the polyol coating portion 14.
- the coated surface of (Y) is pasted together.
- the winding section 152 winds up the laminated film 11 a bonded by the bonding section 151 .
- the lamination section 151 has a pair of lamination rolls R1 and R2, as shown in FIG.
- the lamination rolls R1 and R2 sandwich and bond the first film W1 and the second film W2, and convey them.
- the two laminate rolls R1 and R2 are kept at a constant temperature on the outer peripheral surface by a temperature control unit (not shown). This stabilizes the curing of the two-component curing adhesive.
- the lamination unit 151 passes the first film W1 and the second film W2 between two laminate rolls R1 and R2 arranged opposite to each other, and sends them out from the polyisocyanate coating unit 12.
- the coated surface of the first film W1 fed from the first film W1 and the coated surface of the second film W2 delivered from the polyol coating unit 14 are brought into contact with each other and bonded together.
- the polyisocyanate composition (X) applied to the first film W1 and the polyol composition (Y) applied to the second film W2 are mixed to form a two-component curing adhesive. Curing of the agent is started, and the first film W1 and the second film W2 are attached and fixed.
- the winding section 152 winds up the laminated film 11a formed by bonding the first film W1 and the second film W2 together in the bonding section 151 .
- the method for manufacturing the laminated film 11a of the present embodiment includes a two-liquid separate coating process and an adhesive layer forming process. In this embodiment, the two-liquid separate application step and the adhesive layer forming step are performed continuously.
- the two-liquid separate application step includes a first application step of applying a polyisocyanate composition (X) containing a polyisocyanate (A) and having an elongational viscosity of 0.1 to 10 Pa s on the first film W1, and a polyol ( B) and a second coating step of coating the second film W2 with the polyol composition (Y) having an extensional viscosity of 0.1 to 10 Pa ⁇ s.
- the first coating process and the second coating process are performed simultaneously.
- first coating process A method of performing the first coating step using the laminated film manufacturing apparatus 1 shown in FIGS. 2 to 4 will be described.
- the first film W1 is delivered from the first unwinding section 11 to the polyisocyanate coating section 12 .
- each roll is rotated in the direction indicated by the arrow in FIG.
- the polyisocyanate composition (X) stored in the liquid reservoir 120 is applied to the surface of the doctor roll 122 .
- the temperature of the polyisocyanate composition (X) stored in the liquid reservoir 120 is preferably adjusted to 25° C. to 80° C., preferably 25° C. to 40° C., by a temperature control unit (not shown). is more preferable.
- the shear viscosity of the polyisocyanate composition (X) at 40° C. is preferably 3000 mPa ⁇ s or less, more preferably 2000 mPa ⁇ s or less.
- the polyisocyanate composition (X) applied to the doctor roll 122 is sequentially transferred to the metering roll 123 and the coating roll 124 .
- Each roll of the polyisocyanate coating section 12 is set so that the rotational speed increases sequentially.
- the coating thickness of the polyisocyanate composition (X) gradually decreases, and the coating roll 124 adjusts the coating thickness (coating amount) to a predetermined level.
- the polyisocyanate composition (X) transferred to the coating roll 124 is transferred to the first film W ⁇ b>1 conveyed between the coating roll 124 and the backing roll 125 . Thereby, the polyisocyanate composition (X) is applied to the first film W1.
- the coating amount of the polyisocyanate composition (X) applied to the first film W1 is preferably 0.5 to 3.0 g/m 2 , more preferably 0.5 to 2 .0 g/ m2 .
- the first film W ⁇ b>1 coated with the polyisocyanate composition (X) is delivered to the bonding device 15 .
- the second film W2 is delivered from the second unwinding section 13 to the polyol coating section .
- the gravure roll 141 and impression cylinder 143 are rotated in the directions indicated by the arrows in FIG.
- the surface of the gravure roll 141 is coated with the polyol composition (Y) in the chamber 142 on the second film W2.
- the coating amount of the polyol composition (Y) applied to the second film W2 is preferably 0.5 to 3.0 g/m 2 , more preferably 0.5 to 2.0 g / m2 .
- the temperature of the polyol composition (Y) stored in the coating liquid tank 144 is preferably adjusted to 25° C. to 80° C., preferably 25° C. to 40° C., by the temperature controller 146. is more preferable.
- the viscosity of the polyol composition (Y) is set to a viscosity suitable for a gravure coating machine.
- the rotation direction of the gravure roll 141 may be forward rotation, which is the same direction as the transport direction of the second film W2, or reverse rotation, which is the opposite direction to the transport direction of the second film W2.
- the gravure roll 141 transfers the polyol composition (Y) to the second film W2 while rotating in the direction opposite to the conveying direction of the second film W2.
- the appearance of the polyol composition (Y) applied to the second film W2 can be made good without vertical streaks, roll marks, and the like.
- the second film W ⁇ b>2 coated with the polyol composition (Y) is delivered to the bonding device 15 .
- Adhesive layer forming step In the adhesive layer forming step, by laminating the first film W1 and the second film W2, the polyisocyanate composition (X) applied on the first film W1 and the polyol applied on the second film It is brought into contact with the composition (Y) to cause a curing reaction.
- the first film W1 and the second film W2 are sandwiched between two lamination rolls R1 and R2 facing each other while being in contact with each other. pass between two laminate rolls R1, R2. Then, the first film W1 and the second film W2 are laminated together by the pressure from the two lamination rolls R1 and R2.
- the temperature of the outer peripheral surfaces of the two laminate rolls R1 and R2 is preferably 40°C to 80°C, more preferably 40°C to 60°C.
- the pressure from the two laminating rolls R1, R2 to the first film W1 and the second film W2 can be, for example, 3-300 kg/cm 2 .
- the coated surface of the first film W1 delivered from the polyisocyanate coating unit 12 and the second film delivered from the polyol coating unit 14 are sandwiched between the two lamination rolls R1 and R2.
- the coated surface of W2 contacts.
- the polyisocyanate composition (X) applied to the first film W1 and the polyol composition (Y) applied to the second film W2 are mixed, and curing of the two-component curable adhesive is started. be.
- the laminated film 11a having the adhesive layer 10 between the first film W1 and the second film W2 is obtained.
- the laminated film 11a produced by bonding the first film W1 and the second film W2 together in the bonding section 151 is conveyed to the winding section 152 .
- the laminated film 11 a conveyed to the winding section 152 is wound by the winding section 152 .
- the film transport speed (the winding speed of the laminated film 11a in the winding unit 152) when manufacturing the laminated film 11a can be set to, for example, 30 to 300 m/min. preferably 100 to 250 m/min.
- misting with the polyisocyanate composition (X) and the polyol composition (Y) can suppress the occurrence of Therefore, even if the film conveying speed is 30 m/min or more, the workability is not deteriorated due to the misting of the two-component curing adhesive.
- the laminated film can be efficiently produced continuously at a high film transport speed of 30 m/min or more. If the film conveying speed exceeds 300 m/min, coating problems other than misting, problems during the transfer itself, problems during lamination, and the like may occur. Therefore, it is preferable to set the film transport speed to 300 m/min or less.
- the laminated film 11a obtained by the manufacturing method of the present embodiment is obtained by bonding the first film W1 and the second film W2 together in the bonding section 151, and after being wound up by the winding section 152, is allowed to stand at room temperature as necessary.
- aging is performed by storing for 3 to 48 hours under heating. By performing aging, the two-component curing adhesive is sufficiently cured, and practical physical properties as the adhesive layer 10 may be exhibited.
- the aging time can be shortened because the polyisocyanate composition (X) and the polyol composition (Y) use a two-component curing adhesive having a specific elongational viscosity and excellent initial cohesive strength.
- the manufacturing method of the present embodiment has a wide selection of manufacturing processes, and can improve work efficiency.
- the manufacturing apparatus 1 of the laminated film 11a of the present embodiment includes a polyisocyanate coating unit 12 that applies a polyisocyanate composition (X) having an elongational viscosity of 0.1 to 10 Pa s to the first film W1, and an elongational viscosity A polyol coating portion 14 for applying a polyol composition (Y) having a value of 0.1 to 10 Pa s on the second film W2, a polyisocyanate composition (X) coated surface of the first film W1, and a second and a laminating device 15 for laminating the film W2 with the surface coated with the polyol composition (Y). Therefore, the manufacturing apparatus 1 of the laminated film 11a of the present embodiment uses the liquid-curable adhesive of the present embodiment and manufactures the laminated film 11a by the manufacturing method of the present embodiment having a two-liquid separate application process. can be preferably used.
- the polyisocyanate coating unit 12 applies the polyisocyanate composition (X) having an extensional viscosity of 0.1 to 10 Pa s to the first film W1. and the polyol coating section 14 applies the polyol composition (Y) having an extensional viscosity of 0.1 to 10 Pa ⁇ s to the second film W2. Therefore, in the manufacturing apparatus 1 of the laminated film 11a of the present embodiment, the polyisocyanate composition (X)-coated surface of the first film W1 and the polyol composition (Y)-coated surface of the second film W2 are attached. Misting of the two-component curable adhesive is less likely to occur in the pasting device. Therefore, by using the manufacturing apparatus 1 for the laminated film 11a of the present embodiment, the laminated film 11a can be efficiently produced at a continuously high film transport speed.
- the polyol coating section 14 may be equipped with a gravure coater with a wide range of selection such as the viscosity of the polyol composition (Y), or a roll coater with which misting of the polyol composition (Y) is likely to occur. may be provided, and the options for the coating device for the polyol composition (Y) in the polyol coating section 14 can be increased.
- the viscosity of the polyol composition (Y) is low and problems such as dripping may occur with a roll coater. However, dripping does not occur, and coating quality can be improved to manufacture a high-quality laminated film 11a. Moreover, by using a gravure coater, the configuration of the polyol coating section 14 can be simplified, and the manufacturing apparatus for the laminated film 11a can be miniaturized.
- a roll coater is used in the polyisocyanate coating section 12 that applies the relatively high viscosity polyisocyanate composition (X) to the first film W1.
- a roll coater it is possible to apply even when the viscosity of the polyisocyanate composition (X) is relatively high, and the range of selection of the material of the polyisocyanate composition (X) is widened.
- the method for producing the laminated film 11a of the present embodiment comprises a first coating step of applying the polyisocyanate composition (X) having an elongational viscosity of 0.1 to 10 Pa ⁇ s to the first film W1, and By laminating the first film W1 and the second film W2, and a two-liquid separate coating step consisting of a second coating step of applying the polyol composition (Y) of 1 to 10 Pa s to the second film W2. and an adhesive layer forming step of contacting the polyisocyanate composition (X) applied on the first film W1 and the polyol composition (Y) applied on the second film W2 to cause a curing reaction. .
- the step of mixing the polyisocyanate composition (X) and the polyol composition (Y) is not required. Therefore, the workability is excellent as compared with the case of having a step of mixing the polyisocyanate composition (X) and the polyol composition (Y).
- the polyisocyanate composition (X) and the polyol composition (Y) are not mixed, there is no limitation due to the pot life of the two-component curing adhesive, and the two-component curing adhesive of the present embodiment, which cures quickly. drug can be used.
- the polyisocyanate composition (X) having an elongational viscosity of 0.1 to 10 Pa s is applied to the first film
- a polyol composition (Y) having an elongational viscosity of 0.1 to 10 Pa ⁇ s is applied to the second film W2. Therefore, in the method for producing the laminated film 11a of the present embodiment, the polyisocyanate composition (X) applied on the first film and the polyol composition (Y) applied on the second film are brought into contact.
- misting of the two-component curing adhesive is less likely to occur, and the laminated film can be efficiently produced at a continuously high film transport speed.
- a roll coater is used as the polyisocyanate-coated portion 12, but when the viscosity of the polyisocyanate composition (X) is low, etc., a gravure coater may be used as the polyisocyanate-coated portion 12. . Further, in the above-described embodiment, a gravure coater is used as the polyol-coated portion 14, but a roll coater may be used as the polyol-coated portion 14 when the polyol composition (Y) can be applied. .
- the temperature of the polyol composition (Y) stored in the coating liquid tank 144 is adjusted by the temperature controller 146. Furthermore, the temperature of the polyol composition (Y) stored in the storage section 142a of the chamber 142 and/or the temperature of the gravure roll 141 may be adjusted. Thereby, the viscosity of the polyol composition (Y) during coating can be further stabilized, and the coating quality and the quality of the laminated film 11a can be further improved.
- the polyol coating section 14 that applies the polyol composition (Y) to the second film W2 and the An example of manufacturing the laminated film 11a by a production method having a two-liquid separate application process using the laminated film 11a production apparatus 1 having the laminating device 15 for laminating the first film W1 and the second film W2.
- the laminated film 11a may be manufactured by a manufacturing method having a two-liquid mixing coating process using the manufacturing apparatus shown below, for example.
- FIG. 5 is a front view for explaining another example of the manufacturing apparatus used for manufacturing the laminated film of this embodiment.
- a laminated film manufacturing apparatus 1A shown in FIG. the apparatus forms the adhesive layer 10 between the first film W1 and the second film W2, and manufactures the laminated film 11a of the present embodiment, which is wound into a roll.
- the laminated film manufacturing apparatus 1A shown in FIG. 5 includes, as shown in FIG. . 5 differs from the laminated film manufacturing apparatus 1 shown in FIG. 2 in that a mixture coating section 12A is provided instead of the polyisocyanate coating section 12; It is only the portion without the polyol coating section 14 in the laminated film manufacturing apparatus 1 shown in FIG. In the laminated film manufacturing apparatus 1A shown in FIG. 5, the same members as those in the laminated film manufacturing apparatus 1 shown in FIG.
- the laminated film manufacturing apparatus 1A shown in FIG. 5 is provided with a mixing device (not shown) for mixing the polyisocyanate composition (X) and the polyol composition (Y) of the two-component curing adhesive. Further, in the laminated film manufacturing apparatus 1A shown in FIG. 5, instead of the polyisocyanate supplying section of the laminated film manufacturing apparatus 1 shown in FIG. is provided.
- the following manufacturing method can be used.
- the first film W1 is delivered from the first unwinding section 11 to the mixed liquid coating section 12A.
- each roll is rotated in the direction indicated by the arrow in FIG.
- the mixed liquid of the polyisocyanate composition (X) and the polyol composition (Y) stored in the liquid reservoir 120 is applied to the surface of the doctor roll 122 .
- the temperature of the mixed liquid stored in the liquid reservoir 120 is preferably adjusted to 25° C. to 80° C., more preferably 25° C. to 40° C., by a temperature control unit (not shown). .
- the shear viscosity of the mixture at 40° C. is preferably 2000 mPa ⁇ s or less, more preferably 1800 mPa ⁇ s or less.
- the polyol composition (Y) and the polyisocyanate composition (X) are mixed in the mixing device to initiate curing of the two-component curing adhesive.
- the mixed liquid applied to the doctor roll 122 is sequentially transferred to the metering roll 123 and the coating roll 124 .
- the mixed liquid transferred to the coating roll 124 is transferred to the first film W ⁇ b>1 conveyed between the coating roll 124 and the backing roll 125 .
- the mixed liquid is applied to the first film W1.
- the coating amount of the mixture applied to the first film W1 is preferably 0.5 to 3.0 g/m 2 , more preferably 0.5 to 2.0 g/m 2 . is.
- the first film W1 coated with the mixed liquid in the mixed liquid coating section 12A is delivered to the bonding device 15 as shown in FIG.
- the laminating unit 151 of the laminating device 15 As shown in FIG. 5, two laminates are arranged facing each other in a state where the surface of the first film W1 coated with the liquid mixture is in contact with the second film W2. It is sandwiched between rolls R1 and R2 and passes between the two laminating rolls R1 and R2. Then, the first film W1 and the second film W2 are laminated together by the pressure from the two lamination rolls R1 and R2.
- the temperature of the outer peripheral surfaces of the two laminate rolls R1 and R2 is preferably 40°C to 80°C, more preferably 40°C to 60°C.
- the pressure from the two laminating rolls R1, R2 to the first film W1 and the second film W2 can be, for example, 3-300 kg/cm 2 .
- the laminated film 11a having the adhesive layer 10 between the first film W1 and the second film W2 is obtained.
- the laminated film 11a produced by bonding the first film W1 and the second film W2 together in the bonding section 151 is conveyed to the winding section 152 .
- the laminated film 11 a conveyed to the winding section 152 is wound by the winding section 152 .
- the film transport speed (the winding speed of the laminated film 11a in the winding unit 152) when manufacturing the laminated film 11a can be set to, for example, 30 to 300 m/min. preferably 100 to 250 m/min.
- the laminated film 11a is produced using the two-component curing adhesive of the present embodiment, misting by the mixed liquid which is the component containing the polyol composition (Y) can be suppressed. Therefore, even if the film transport speed is 30 m/min or more, the misting of the mixed solution does not lower the workability.
- the laminated film can be efficiently produced continuously at a high film transport speed of 30 m/min or more. If the film conveying speed exceeds 300 m/min, coating problems other than misting, problems during the transfer itself, problems during lamination, and the like may occur. Therefore, it is preferable to set the film transport speed to 300 m/min or less.
- the laminated film 11a of the present embodiment is manufactured using the two-component curing adhesive of the present embodiment, the mixed liquid, which is a component containing the polyol composition (Y), is applied onto the second film W2.
- misting due to the polyol composition (Y) is less likely to occur. Therefore, the laminated film 11a of the present embodiment can be efficiently manufactured using a manufacturing method having a two-liquid mixing coating process.
- the laminated film 11a is formed by using a manufacturing method having a two-component separate coating process including a step of coating only the polyol composition (Y) on the film as the manufacturing method having the two-component separate coating process.
- a manufacturing method having a two-component separate coating process including a step of coating only the polyol composition (Y) on the film as the manufacturing method having the two-component separate coating process.
- a mixed solution of the polyisocyanate composition and the polyol composition is applied onto the first film
- a solution containing a curing accelerator is applied onto the second film.
- a mixture of a part of the polyol composition and the polyisocyanate composition is applied on the first film
- the remainder of the polyol composition and the curing accelerator are applied.
- the solution containing is applied to the second film.
- Polyisocyanate composition (X-1) [Production of polyisocyanate (A)] 41.9 parts of 4,4-diphenylmethane diisocyanate (hereinafter abbreviated as "MDI") and 13.0 parts of 2,4'-MDI were added to a flask equipped with a stirrer, a thermometer, and a nitrogen gas inlet tube. and 0.1 part of xylylene diisocyanate were placed in a reaction vessel, stirred under nitrogen gas, and heated to 60°C.
- MDI 4,4-diphenylmethane diisocyanate
- a polyisocyanate composition (X-1) composed of the polyisocyanate (A) was obtained by adding dropwise in batches and stirring at 80° C. for 5 to 6 hours to cause a urethanization reaction.
- the isocyanate content of polyisocyanate (A) was measured by a titration method using di-n-butylamine. As a result, it was 14% by mass. Moreover, the melt shear viscosity at 40° C. was measured for the polyisocyanate (A). As a result, it was 1500 mPa ⁇ s.
- Polyisocyanate composition (X-2, X-3) As the polyisocyanate compositions X-2 and X-3, the following were prepared. X-2: 2K-SF-220A (manufactured by DIC Corporation), isocyanate content (14% by mass) X-3: 2K-SF-700A (manufactured by DIC Corporation), isocyanate content (21% by mass)
- Polyol Compositions (Y-1) to (Y-6) The polyol (B), polyamine (C) and additives shown in Table 1 were mixed in the proportions shown in Table 1 to obtain polyol compositions (Y-1) to (Y-6).
- EC310 Polyoxypropylene polyamine (manufactured by BASF) Baxxdur EC310 "catalyst” ⁇ -caprolactam: 2-oxohexamethyleneimine (manufactured by Kanto Chemical Co., Ltd.) ⁇ -valerolactam: tetrahydro-2H-pyran-2-one (manufactured by Kanto Chemical Co., Ltd.) DBTDL: Dibutyltin dilaurate (manufactured by Nitto Kasei Co., Ltd.) Neostan U-100 Bi-Zn: mixed catalyst of bismuth neodecanoate and zinc neodecanoate (manufactured by The Shepherd Chemical Company) Bicat 8108/Z mixture "adhesion promoter" OFS-6040: 3-glycidyloxypropyltrimethoxysilane (manufactured by Dow Corning Toray Co., Ltd.) KBM903:
- the hydroxyl value or amine value of the materials used in the polyol compositions (Y-1) to (Y-8) was determined by the method shown below.
- the hydroxyl value was obtained according to the hydroxyl value measurement method of JIS-K0070.
- the amine value was determined according to ASTM D2073 Amine Value Standard Test Method. Then, the sum of the hydroxyl value and the amine value contained in the polyol compositions (Y-1) to (Y-8) was determined. The results are shown in Tables 1 and 2.
- the elongational viscosity at an elongation speed of 4000 s -1 was measured by the method shown below. .
- Table 2 shows the results.
- the elongational viscosity was measured according to the capillary rheometer evaluation method described in JIS-7199 (ISO 11443, ASTM D 3835).
- a capillary die with a length of 10 mm and a diameter of 0.5 mm and a capillary die with a length of 0.25 mm and a diameter of 0.5 mm were used.
- a temperature of 40° C. and a shear rate of 1000-300000 s ⁇ 1 the pressure drop was removed using the Bergley correction to obtain the true shear viscosity.
- the elongation velocity and the corresponding elongation viscosity were determined using the Cogswell equation.
- Examples 1 to 7, Comparative Examples 1 to 3 Polyisocyanate compositions (X-1) to (X-3) and polyol compositions (Y-1) to (Y-8) were used in the proportions shown in Table 2, and the 2 to 4, laminated films of Examples 1 to 7 and Comparative Examples 1 to 3 were produced at film transport speeds of 100, 150, 200 and 250 m/min, respectively.
- the ratios of the polyisocyanate compositions (X-1) to (X-3) and the polyol compositions (Y-1) to (Y-8) are the polyisocyanate compositions (X-1) to
- the molar ratio of the isocyanate group of (X-3) to the sum of the hydroxyl value and amine value of the polyol compositions (Y-1) to (Y-8) [isocyanate group/(hydroxyl value + amine value) ] is in the range of 1.4 to 1.6.
- the molar ratio is described as the NCO excess.
- the functional group content of the polyisocyanate composition shown in Table 2 is the isocyanate content (%) of the polyisocyanate compositions (X-1) to (X-3).
- the functional group content of the polyol composition described in Table 2 is the sum of the hydroxyl value and amine value of the polyol composition (mgKOH/g).
- One of the polyisocyanate compositions (X-1) to (X-3) was applied to the corona-treated surface of a 12 ⁇ m-thick single-sided corona-treated PET film (first film) with a roll coater (first coating process).
- first coating process the temperature of the polyisocyanate composition (X) stored in the coating liquid tank was set to 40°C.
- any one of the polyol compositions (Y-1) to (Y-8) was applied to the aluminum-deposited surface of a 25 ⁇ m-thick aluminum-deposited polypropylene (VMCPP) film (second film) with a gravure coater. applied (second application step).
- the total coating amount of the polyisocyanate compositions (X-1) to (X-3) and the polyol compositions (Y-1) to (Y-8) is 2. 0 g/m 2 .
- the first coated portion and the second coated portion during coating were visually observed, and the misting properties were evaluated according to the criteria described later.
- the adhesive layer forming process was performed continuously from the first coating process and the second coating process.
- the adhesive layer forming step by laminating the first film and the second film, any of the polyisocyanate compositions (X-1) to (X-3) applied on the first film and the second It was carried out by contacting any one of the polyol compositions (Y-1) to (Y-8) coated on the film to cause a curing reaction.
- the misting property in the process was evaluated, and 3 or more was regarded as acceptable.
- Table 2 shows the results. (Evaluation of misting property) 4: No misting occurs in both the first and second coating parts 3: Some misting occurs in both the first and second coating parts 2: First coating part 1: Severe misting occurs in both the first and second coating parts
- the laminate film was cut into strips having a width of 10 mm and a length of 200 mm, and only the first film was cut in the width direction from the first film side surface. Then, only the second film was cut in the width direction from the second film side of the laminated film at a position spaced 10 mm in the length direction in plan view from the cutting position of the first film. This gave a test piece having an adhesive layer with a plane area of 10 mm 2 between the cutting position of the first film and the cutting position of the second film.
- One end of the obtained test piece in the length direction is held by a clamp, and the other end is pulled in the length direction at a speed of 5 mm / min using a tensile tester (Autograph AGS-J, manufactured by Shimadzu Corporation), The shear strength was measured.
- Comparative Example 1 in which the polyisocyanate composition (X) had an elongational viscosity of more than 10 Pa s
- Comparative Example 2 in which the polyol composition (Y) had an elongational viscosity of more than 10 Pa s
- the film transport speed was 100 m/ Even at min, some misting occurred.
- Comparative Example 3 in which the polyisocyanate composition (X) and the polyol composition (Y) had extensional viscosities of more than 10 Pa ⁇ s, misting occurred even when the film transport speed was 100 m/min.
- Comparative Example 1 the shear strength was less than 1 N/10 mm even after 24 hours had passed since the end of the adhesive layer forming process. Moreover, in Comparative Example 2, the shear strength was less than 10 N/10 mm even after 12 hours had passed since the end of the adhesive layer forming step. Moreover, in Comparative Example 3, the shear strength was less than 5 N/10 mm even after 24 hours had passed since the end of the adhesive layer forming step. From this, it was confirmed that in Comparative Examples 1 to 3, the shear strength did not increase at an early stage, and the initial cohesive strength was inferior to that in Examples 1 to 7.
- the laminated film obtained using the two-component curing adhesive of the present invention has excellent initial cohesive strength, is less prone to misting during its production, and has excellent properties. It can be manufactured efficiently.
- 1 laminated film manufacturing apparatus, 10: adhesive layer, 11: first unwinding section, 11a: laminated film, 12: polyisocyanate coating section (first coating section), 13: second unwinding section, 14: Polyol coating part (second coating part), 15: Bonding device, 111: Film mounting part, 120: Liquid reservoir part, 121: Application roll, 122: Doctor roll, 123: Metering roll, 124: Coating roll, 125: backing roll, 126: barrier plate, 131: film mounting part, 141: gravure roll, 142: chamber, 142a: storage part, 142b: doctor blade, 142c: seal plate, 142d: side plate, 143: Impression cylinder, 144: Coating liquid tank, 145: Pump, 146: Temperature controller, 151: Bonding unit, 152: Winding unit, R1, R2: Lamination roll, W1: First film, W2: Second film .
Landscapes
- Chemical & Material Sciences (AREA)
- Organic Chemistry (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Adhesives Or Adhesive Processes (AREA)
- Adhesive Tapes (AREA)
- Fixed Capacitors And Capacitor Manufacturing Machines (AREA)
Priority Applications (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US17/601,513 US11525074B2 (en) | 2021-02-15 | 2021-02-15 | Two-component curing adhesive, laminated film, laminated film-manufacturing apparatus, and method for manufacturing laminated film |
| JP2021553276A JP7136364B1 (ja) | 2021-02-15 | 2021-02-15 | 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 |
| PCT/JP2021/005515 WO2022172448A1 (ja) | 2021-02-15 | 2021-02-15 | 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 |
| EP21777613.7A EP4071222A4 (en) | 2021-02-15 | 2021-02-15 | TWO-COMPONENT CURING ADHESIVE, LAMINATED FILM, LAMINATED FILM MANUFACTURING DEVICE AND METHOD FOR MANUFACTURING A LAMINATED FILM |
| CN202180003072.XA CN115413294A (zh) | 2021-02-15 | 2021-02-15 | 双组分固化型粘接剂、层叠薄膜、层叠薄膜制造装置、层叠薄膜的制造方法 |
| TW111104783A TWI792909B (zh) | 2021-02-15 | 2022-02-09 | 二液硬化型接著劑、積層膜、積層膜製造裝置、積層膜之製造方法 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/JP2021/005515 WO2022172448A1 (ja) | 2021-02-15 | 2021-02-15 | 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2022172448A1 true WO2022172448A1 (ja) | 2022-08-18 |
Family
ID=82801107
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2021/005515 Ceased WO2022172448A1 (ja) | 2021-02-15 | 2021-02-15 | 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US11525074B2 (cg-RX-API-DMAC7.html) |
| EP (1) | EP4071222A4 (cg-RX-API-DMAC7.html) |
| JP (1) | JP7136364B1 (cg-RX-API-DMAC7.html) |
| CN (1) | CN115413294A (cg-RX-API-DMAC7.html) |
| TW (1) | TWI792909B (cg-RX-API-DMAC7.html) |
| WO (1) | WO2022172448A1 (cg-RX-API-DMAC7.html) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2024089905A (ja) * | 2022-12-22 | 2024-07-04 | Dic株式会社 | 接着剤、積層体、電池用包装材及び電池 |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2000509425A (ja) * | 1996-05-16 | 2000-07-25 | ミネソタ マイニング アンド マニュファクチャリング カンパニー | 接着剤組成物と使用方法 |
| JP2003171642A (ja) | 2001-12-03 | 2003-06-20 | Sekisui Chem Co Ltd | 二液分別塗布型ウレタン系接着剤 |
| JP2003171643A (ja) | 2001-12-03 | 2003-06-20 | Sekisui Chem Co Ltd | 二液分別塗布型ウレタン系接着剤 |
| JP2003171641A (ja) | 2001-12-04 | 2003-06-20 | Sekisui Chem Co Ltd | 二液分別塗布型ウレタン系接着剤 |
| WO2018043470A1 (ja) * | 2016-09-05 | 2018-03-08 | Dic株式会社 | 軟包装用フィルムの製造方法 |
| WO2018043469A1 (ja) * | 2016-09-05 | 2018-03-08 | Dic株式会社 | 軟包装用フィルムの製造方法 |
| JP2018520218A (ja) * | 2015-05-05 | 2018-07-26 | スリーエム イノベイティブ プロパティズ カンパニー | 温めると溶ける光学的に透明な接着剤及びそのディスプレイアセンブリ用途 |
| JP2019533034A (ja) * | 2016-09-29 | 2019-11-14 | Dic株式会社 | 接着剤、それを使用した積層フィルム、及び接着剤用ポリオール組成物 |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP6753210B2 (ja) | 2016-08-22 | 2020-09-09 | 東洋インキScホールディングス株式会社 | 接着剤組成物 |
| TWI796450B (zh) * | 2018-03-23 | 2023-03-21 | 日商迪愛生股份有限公司 | 接著劑、積層薄膜、及積層薄膜之製造方法 |
| JP7004090B2 (ja) * | 2018-12-21 | 2022-01-21 | Dic株式会社 | 接着剤、積層フィルム、及び積層フィルムの製造方法 |
-
2021
- 2021-02-15 US US17/601,513 patent/US11525074B2/en active Active
- 2021-02-15 WO PCT/JP2021/005515 patent/WO2022172448A1/ja not_active Ceased
- 2021-02-15 CN CN202180003072.XA patent/CN115413294A/zh active Pending
- 2021-02-15 EP EP21777613.7A patent/EP4071222A4/en not_active Withdrawn
- 2021-02-15 JP JP2021553276A patent/JP7136364B1/ja active Active
-
2022
- 2022-02-09 TW TW111104783A patent/TWI792909B/zh active
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2000509425A (ja) * | 1996-05-16 | 2000-07-25 | ミネソタ マイニング アンド マニュファクチャリング カンパニー | 接着剤組成物と使用方法 |
| JP2003171642A (ja) | 2001-12-03 | 2003-06-20 | Sekisui Chem Co Ltd | 二液分別塗布型ウレタン系接着剤 |
| JP2003171643A (ja) | 2001-12-03 | 2003-06-20 | Sekisui Chem Co Ltd | 二液分別塗布型ウレタン系接着剤 |
| JP2003171641A (ja) | 2001-12-04 | 2003-06-20 | Sekisui Chem Co Ltd | 二液分別塗布型ウレタン系接着剤 |
| JP2018520218A (ja) * | 2015-05-05 | 2018-07-26 | スリーエム イノベイティブ プロパティズ カンパニー | 温めると溶ける光学的に透明な接着剤及びそのディスプレイアセンブリ用途 |
| WO2018043470A1 (ja) * | 2016-09-05 | 2018-03-08 | Dic株式会社 | 軟包装用フィルムの製造方法 |
| WO2018043469A1 (ja) * | 2016-09-05 | 2018-03-08 | Dic株式会社 | 軟包装用フィルムの製造方法 |
| JP2019533034A (ja) * | 2016-09-29 | 2019-11-14 | Dic株式会社 | 接着剤、それを使用した積層フィルム、及び接着剤用ポリオール組成物 |
Non-Patent Citations (2)
| Title |
|---|
| "Paint Raw Material Handbook", 1970, JAPAN PAINT MANUFACTURERS ASSOCIATION |
| See also references of EP4071222A4 |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2024089905A (ja) * | 2022-12-22 | 2024-07-04 | Dic株式会社 | 接着剤、積層体、電池用包装材及び電池 |
| JP7904527B2 (ja) | 2022-12-22 | 2026-08-13 | Dic株式会社 | 接着剤、積層体、電池用包装材及び電池 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7136364B1 (ja) | 2022-09-13 |
| EP4071222A4 (en) | 2023-01-25 |
| TWI792909B (zh) | 2023-02-11 |
| CN115413294A (zh) | 2022-11-29 |
| US11525074B2 (en) | 2022-12-13 |
| TW202244232A (zh) | 2022-11-16 |
| US20220259472A1 (en) | 2022-08-18 |
| EP4071222A1 (en) | 2022-10-12 |
| JPWO2022172448A1 (cg-RX-API-DMAC7.html) | 2022-08-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP7004090B2 (ja) | 接着剤、積層フィルム、及び積層フィルムの製造方法 | |
| CN111886313B (zh) | 粘接剂、层叠膜和层叠膜的制造方法 | |
| US11180685B2 (en) | Adhesive, laminated film using thereof and polyol composition for adhesive | |
| JP6512256B2 (ja) | 2液硬化型ラミネート接着剤、その硬化物、積層フィルムの製造方法、及び2液硬化型ラミネート接着剤用アミン溶液 | |
| CN114222800A (zh) | 异氰酸酯系粘接剂 | |
| CN109983097A (zh) | 反应型粘接剂、层叠膜及包装体 | |
| JP7003572B2 (ja) | 無溶剤型ラミネート接着剤、その硬化物、積層体及び包装体 | |
| CN110475835A (zh) | 双组份型粘接剂用的固化剂、双组份型粘接剂、层叠膜和包装体 | |
| JP7136364B1 (ja) | 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 | |
| JP7332066B2 (ja) | 積層フィルム製造装置、積層フィルムの製造方法、二液硬化型接着剤、積層フィルム | |
| CN111819261A (zh) | 软包装用膜的制造方法 | |
| JP7136363B1 (ja) | 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 | |
| JP7343063B2 (ja) | 積層フィルム製造装置、積層フィルムの製造方法、二液硬化型接着剤、積層フィルム | |
| WO2022172839A1 (ja) | 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 | |
| WO2022172841A1 (ja) | 二液硬化型接着剤、積層フィルム、積層フィルム製造装置、積層フィルムの製造方法 | |
| JP2011116917A (ja) | ドライラミネート用接着剤 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| ENP | Entry into the national phase |
Ref document number: 2021553276 Country of ref document: JP Kind code of ref document: A |
|
| ENP | Entry into the national phase |
Ref document number: 2021777613 Country of ref document: EP Effective date: 20211006 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |