WO2022014612A1 - 排気管 - Google Patents
排気管 Download PDFInfo
- Publication number
- WO2022014612A1 WO2022014612A1 PCT/JP2021/026359 JP2021026359W WO2022014612A1 WO 2022014612 A1 WO2022014612 A1 WO 2022014612A1 JP 2021026359 W JP2021026359 W JP 2021026359W WO 2022014612 A1 WO2022014612 A1 WO 2022014612A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- porous layer
- inorganic porous
- mass
- less
- exhaust pipe
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/01—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics
- C04B35/46—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics based on titanium oxides or titanates
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/71—Ceramic products containing macroscopic reinforcing agents
- C04B35/78—Ceramic products containing macroscopic reinforcing agents containing non-metallic materials
- C04B35/80—Fibres, filaments, whiskers, platelets, or the like
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B38/00—Porous mortars, concrete, artificial stone or ceramic ware; Preparation thereof
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B41/00—After-treatment of mortars, concrete, artificial stone or ceramics; Treatment of natural stone
- C04B41/80—After-treatment of mortars, concrete, artificial stone or ceramics; Treatment of natural stone of only ceramics
- C04B41/81—Coating or impregnation
- C04B41/85—Coating or impregnation with inorganic materials
- C04B41/87—Ceramics
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C24/00—Coating starting from inorganic powder
- C23C24/08—Coating starting from inorganic powder by application of heat or pressure and heat
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N13/00—Exhaust or silencing apparatus characterised by constructional features
- F01N13/08—Other arrangements or adaptations of exhaust conduits
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N13/00—Exhaust or silencing apparatus characterised by constructional features
- F01N13/14—Exhaust or silencing apparatus characterised by constructional features having thermal insulation
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01N—GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR MACHINES OR ENGINES IN GENERAL; GAS-FLOW SILENCERS OR EXHAUST APPARATUS FOR INTERNAL-COMBUSTION ENGINES
- F01N13/00—Exhaust or silencing apparatus characterised by constructional features
- F01N13/16—Selection of particular materials
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16L—PIPES; JOINTS OR FITTINGS FOR PIPES; SUPPORTS FOR PIPES, CABLES OR PROTECTIVE TUBING; MEANS FOR THERMAL INSULATION IN GENERAL
- F16L9/00—Rigid pipes
- F16L9/14—Compound tubes, i.e. made of materials not wholly covered by any one of the preceding groups
Definitions
- Patent Document 1 Japanese Patent Application Laid-Open No. 2018-031346 (hereinafter referred to as Patent Document 1) describes an exhaust pipe of an internal combustion engine in which an inorganic porous layer (heat insulating material) is arranged between a metal inner pipe and a metal outer pipe. It has been disclosed.
- an inorganic porous layer is provided between the inner pipe and the outer pipe to insulate the space between the inner pipe and the outer pipe, and the temperature of the exhaust gas flowing into the catalyst provided downstream of the exhaust pipe. The decline is suppressed. By suppressing the temperature drop of the exhaust gas flowing into the catalyst, the warm-up of the catalyst is completed at an early stage.
- the inorganic porous layer When the inorganic porous layer is arranged between the double pipes as in Patent Document 1, the exhaust gas does not come into direct contact with the inorganic porous layer. Therefore, the inorganic porous layer only needs to have heat insulating performance.
- the inorganic porous layer is provided inside the inner tube of the double tube or inside the single tube, the exhaust gas comes into direct contact with the inorganic porous layer, and the inorganic porous layer is exposed to a high temperature. Therefore, when the inorganic porous layer is provided at the portion through which the exhaust gas passes, it is necessary to improve the thermal impact resistance of the inorganic porous layer. It is an object of the present specification to provide a novel exhaust pipe in which an inorganic porous layer is provided at a portion through which the exhaust gas of the metal pipe passes.
- the exhaust pipe disclosed in the present specification may include a metal pipe and an inorganic porous layer provided at a portion of the inner surface of the metal pipe through which the exhaust gas passes.
- the inorganic porous layer contains ceramic fibers and is composed of 15% by mass or more of an alumina component and 45% by mass or more of a titania component, and the titania component may contain a rutile-type crystal phase. ..
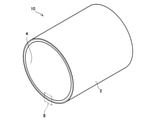
- the perspective view of the exhaust pipe is shown.
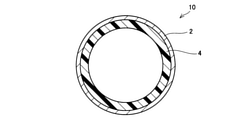
- a partially enlarged view of the exhaust pipe is shown.
- the sectional view of the exhaust pipe is shown.
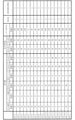
- the results of the experimental example are shown.
- the results of the experimental example are shown.
- the exhaust pipe disclosed in the present specification includes a metal pipe and an inorganic porous layer provided at a portion of the inner surface of the metal pipe through which the exhaust gas passes.
- the inorganic porous layer may contain ceramic fibers.
- the ceramic fiber can absorb the influence of the difference in the coefficient of thermal expansion between the metal tube and the inorganic porous layer. Specifically, since the inorganic porous layer can be deformed following the deformation (heat expansion, heat contraction) of the metal tube, it is possible to prevent the inorganic porous layer from peeling off from the metal tube. That is, the adhesion between the metal tube and the inorganic porous layer is improved.
- the inorganic porous layer can suppress the exhaust gas from coming into contact with the metal pipe and prevent the metal pipe from deteriorating. Further, since the inorganic porous layer is composed of 15% by mass or more of an alumina component and 45% by mass or more of a titania component, the melting point of the inorganic porous layer itself is high, and the shape changes due to the heat of the exhaust gas. Can also be suppressed.
- the rutile-type crystal phase may be contained in the titania component constituting the inorganic porous layer.
- the titania component may contain an anatase-type crystal phase, a brookite-type crystal phase, and an amorphous phase in addition to the rutile-type crystal phase.
- Rutile-type titania is more stable in high temperature environments than other crystalline and amorphous phases. Specifically, rutile-type titania does not undergo a phase transition even when exposed to high temperatures. Therefore, in the inorganic porous layer containing rutile-type titania, the volume change due to the phase transition is unlikely to occur, and the internal stress is unlikely to occur.
- the rutile-type crystal phase is contained in the titania component constituting the inorganic porous layer, so that the thermal impact resistance of the inorganic porous layer is improved.
- the anatase-type crystal phase and the brookite-type crystal phase undergo a phase transition to the rutile-type crystal phase in a high-temperature environment.
- the titania component may be mainly composed of a rutile-type crystal phase. That is, the rutile-type crystal phase may occupy 50% by mass or more of the titania component. As described above, the rutile-type crystal phase is stable in a high temperature environment. Therefore, if the rutile-type crystal phase occupies 50% by mass or more of the titania component, the thermal impact resistance of the inorganic porous layer is remarkably improved.
- the ratio of the rutile-type crystal phase to the titania component may be 60% by mass or more, 70% by mass or more, 80% by mass or more, and 90% by mass or more. All of the titania components may be rutile-type crystal phases.
- Equation 1 0.5 ⁇ 1 / ⁇ 2 ⁇ 1.2
- the inorganic porous layer may contain flat plate-shaped ceramic particles.
- the plate-shaped ceramic particles By using the plate-shaped ceramic particles, a part of the ceramic fiber can be replaced with the plate-shaped ceramic particles.
- the length of the plate-like ceramic particles (longitudinal size) is shorter than the length of the ceramic fibers. Therefore, by using the plate-shaped ceramic particles, the heat transfer path in the inorganic porous layer is divided, and heat transfer in the inorganic porous layer is less likely to occur. As a result, the heat insulating performance of the inorganic porous layer is further improved.
- the inorganic porous layer may contain granular particles of 0.1 ⁇ m or more and 10 ⁇ m or less. When the inorganic porous layer is formed (baked), the ceramic fibers are bonded to each other via granular particles to obtain a high-strength inorganic porous layer. Further, the thickness of the inorganic porous layer may be 1 mm or more. As a result, the heat insulating property of the exhaust pipe can be sufficiently exhibited. In the exhaust pipe, since the inorganic porous layer contains ceramic fibers, it is possible to realize an inorganic porous layer of 1 mm or more.
- the inorganic porous layer can be formed to 1 mm or more.
- the inorganic porous layer does not contain ceramic fibers, the inorganic porous layer shrinks during the molding process and cracks or the like occur. Therefore, when the inorganic porous layer does not contain ceramic fibers, the inorganic porous layer is inorganic porous. It is difficult to form the quality layer into a thick film of 1 mm or more.
- the inorganic porous layer is composed of an alumina (Al 2 O 3 ) component of 15% by mass or more and 55% by mass or less and a titania (TiO 2 ) component of 45% by mass or more and 85% by mass or less. ..
- the alumina component contained in the inorganic porous layer may be 25% by mass or more, 30% by mass or more, or 40% by mass or more.
- the difference in thermal conductivity between the metal tube and the inorganic porous layer is large.
- the thermal conductivity of the metal tube may be 100 times or more the thermal conductivity of the inorganic porous layer.
- the thermal conductivity of the metal tube may be 150 times or more the thermal conductivity of the inorganic porous layer, 200 times or more the thermal conductivity of the inorganic porous layer, and the heat of the inorganic porous layer.
- the conductivity may be 250 times or more, and the thermal conductivity of the inorganic porous layer may be 300 times or more.
- the thermal conductivity of the metal tube may be 10 W / mK or more and 400 W / mK or less.
- the thermal conductivity of the metal tube may be 25 W / mK or more, 50 W / mK or more, 100 W / mK or more, 150 W / mK or more, and 200 W / mK or more. It may be 250 W / mK or more, 300 W / mK or more, or 380 W / mK or more.
- the thermal conductivity of the metal tube may be 350 W / mK or less, 300 W / mK or less, 250 W / mK or less, 200 W / mK or less, 150 W / mK or less. May be.
- the thermal conductivity of the inorganic porous layer may be 0.05 W / mK or more and 3 W / mK or less.
- the thermal conductivity of the inorganic porous layer may be 0.1 W / mK or more, 0.2 W / mK or more, 0.3 W / mK or more, and 0.5 W / mK or more. It may be 0.7 W / mK or more, 1 W / mK or more, 1.5 W / mK or more, or 2 W / mK or more.
- the thermal conductivity of the inorganic porous layer may be 2.5 W / mK or less, 2.0 W / mK or less, 1.5 W / mK or less, and 1 W / mK or less. It may be 0.5 W / mK or less, 0.3 W / mK or less, and 0.25 W / mK or less.
- the metal pipe may be a single pipe or a multiple pipe (for example, a double pipe).
- the metal tube may be linear, the whole (or a part) may be curved, the intermediate portion may be tapered, or the metal tube may be a branch tube.
- the inorganic porous layer may be provided on the inner surface of the metal tube in the case of a single tube, or on the inner surface of the metal tube arranged on the innermost side in the case of a multiple tube.
- the inorganic porous layer may cover the entire inner surface of the metal tube or a part of the inner surface of the metal tube.
- the inorganic porous layer may cover a portion other than the end portion (one end or both ends) of the metal tube.
- the inorganic porous layer may be made of a uniform material in the thickness direction. That is, the inorganic porous layer may be a single layer. Further, the inorganic porous layer may be composed of a plurality of layers having different compositions in the thickness direction. That is, the inorganic porous layer may have a multi-layer structure in which a plurality of layers are laminated. Alternatively, the inorganic porous layer may have an inclined structure in which the composition gradually changes in the thickness direction.
- the exhaust pipe can be easily manufactured (the step of forming the inorganic porous layer on the inner surface of the metal pipe).
- the characteristics of the inorganic porous layer can be changed in the thickness direction.
- the ratio of the rutile-type crystal phase to the titania component can be made larger than that of other portions.
- the structure of the inorganic porous layer (single layer, multi-layer, inclined structure) can be appropriately selected according to the purpose of use of the exhaust pipe.
- the porosity of the inorganic porous layer may be 45% by volume or more and 90% by volume or less. When the porosity is 45% by volume or more, the heat insulating property can be sufficiently exhibited. Further, when the porosity is 90% by volume or less, sufficient strength can be secured.
- the porosity of the inorganic porous layer may be 55% by volume or more, 60% by volume or more, or 65% by volume or more. Further, the porosity of the inorganic porous layer may be 85% by volume or less, 80% by volume or less, 70% by volume or less, 65% by volume or less, and 60% by volume. It may be as follows.
- the porosity of the inorganic porous layer may be 45% by volume or more and 90% by volume or less as a whole, and the porosity may differ in the thickness direction. .. In this case, there may be a portion having a porosity of less than 45% by volume or a portion having a porosity of more than 90% by volume.
- the thickness of the inorganic porous layer may be 1 mm or more, although it depends on the required performance. When the thickness of the inorganic porous layer is 1 mm or more, the heat insulating property can be sufficiently exhibited. In the case of the inorganic porous layer in which the ceramic fiber is not used, it is difficult to maintain the thickness at 1 mm or more because it shrinks in the manufacturing process (for example, the firing step). Since the inorganic porous layer disclosed in the present specification contains ceramic fibers, shrinkage in the manufacturing process is suppressed, and a thickness of 1 mm or more can be maintained.
- the thickness of the inorganic porous layer may be 30 mm or less, 20 mm or less, 15 mm or less, 10 mm or less, and 5 mm or less.
- the inorganic porous layer is composed of one or more materials of ceramic particles (granular particles), plate-shaped ceramic particles, and ceramic fibers.
- the ceramic particles, the plate-shaped ceramic particles, and the ceramic fibers may contain alumina and / or titania as constituent components.
- the ceramic particles, the plate-shaped ceramic particles, and the ceramic fibers may be formed by alumina and / or titania. That is, the inorganic porous layer may contain 15% by mass or more of an alumina component and 45% by mass or more of a titania component in the entire constituent material (constituting substance).
- the inorganic porous layer contains at least ceramic fibers, although the constituent components are arbitrary (alumina component and titania component may or may not be contained).
- the ceramic particles may be used as a bonding material for joining aggregates forming the skeleton of an inorganic porous layer such as plate-shaped ceramic particles and ceramic fibers.
- the ceramic particles may be granular particles of 0.1 ⁇ m or more and 10 ⁇ m or less.
- the ceramic particles may have a larger particle size due to sintering or the like in the manufacturing process (for example, firing process). That is, as a raw material for producing the inorganic porous layer, the ceramic particles may be granular particles having a size of 0.1 ⁇ m or more and 10 ⁇ m or less (average particle size before firing).
- the ceramic particles may be 0.5 ⁇ m or more, and may be 5 ⁇ m or less.
- a metal oxide may be used as the material of the ceramic particles.
- metal oxide alumina (Al 2 O 3), spinel (MgAl 2 O 4), titania (TiO 2), zirconia (ZrO 2), magnesia (MgO), mullite (Al 6 O 13 Si 2) , cordierite (MgO ⁇ Al 2 O 3 ⁇ SiO 2), yttria (Y 2 O 3), steatite (MgO ⁇ SiO 2), forsterite (2MgO ⁇ SiO 2), lanthanum aluminate (LaAlO 3), strontium titanate (SrTiO 3 ) and the like can be mentioned.
- These metal oxides have high corrosion resistance and can be suitably applied as a protective layer for an exhaust pipe.
- the ceramic particles contain titania particles, the inclusion of the rutile-type crystal phase in the ceramic particles improves the thermal impact resistance of the bonding material that joins the aggregates, and suppresses the deterioration of the inorganic porous layer.
- the plate-shaped ceramic can function as an aggregate or a reinforcing material in the inorganic porous layer. That is, the plate-shaped ceramic, like the ceramic fiber, improves the strength of the inorganic porous layer and further suppresses the shrinkage of the inorganic porous layer in the manufacturing process. By using the plate-shaped ceramic particles, the heat transfer path in the inorganic porous layer can be divided. Therefore, the heat insulating property can be improved as compared with the form in which only the ceramic fiber is used as the aggregate.
- the surface shape (shape observed from the thickness direction) of the flat plate-shaped ceramic particles is not particularly limited, and for example, a polygon such as a rectangle, a substantially circular shape, an irregular shape surrounded by a curved line and / or a straight line is often used.
- the longitudinal size when observing the cross section may be 5 ⁇ m or more and 100 ⁇ m or less. When the size in the longitudinal direction is 5 ⁇ m or more, excessive sintering of the ceramic particles can be suppressed. When the size in the longitudinal direction is 100 ⁇ m or less, the effect of dividing the heat transfer path in the inorganic porous layer can be obtained as described above, and it can be suitably applied to an exhaust pipe used in a high temperature environment.
- the plate-shaped ceramic particles contained in the inorganic porous layer may have an aspect ratio of 10 or more and 60 or less when the cross section is observed by SEM.
- the plate-shaped ceramic particles having a cross-sectional aspect ratio of 10 or more and 60 or less have an aspect ratio in the manufacturing process of the inorganic porous layer by using, for example, plate-shaped ceramic particles having a cross-sectional aspect ratio of 60 or more and 100 or less as a raw material. The ratio becomes smaller and as a result remains in the inorganic porous material.
- the aspect ratio of the cross section is 10 or more, the sintering of the ceramic particles can be satisfactorily suppressed.
- the aspect ratio of the cross section is 10 or more, it is possible to prevent the inorganic porous layer from becoming too hard (the Young's modulus becomes too high) after production (after firing). As a result, it is possible to prevent the inorganic porous layer from being damaged (cracking or the like) due to thermal shock immediately after the start of the internal combustion engine (contact of high-temperature exhaust gas with the inorganic porous in a low temperature state). Further, when the aspect ratio of the cross section is 60 or less, the decrease in the strength of the plate-shaped ceramic particles themselves is suppressed, and the damage of the inorganic porous layer due to the vibration of the exhaust pipe or the gas flow of the exhaust gas can be suppressed. can.
- talc Mg 3 Si 4 O 10 (OH) 2
- minerals such as mica and kaolin, clay, glass and the like. Can also be used.
- the ceramic fiber can function as an aggregate or a reinforcing material in the inorganic porous layer. That is, the ceramic fiber improves the strength of the inorganic porous layer and further suppresses the shrinkage of the inorganic porous layer in the manufacturing process.
- the length of the ceramic fiber may be 50 ⁇ m or more and 200 ⁇ m or less.
- the diameter (average diameter) of the ceramic fiber may be 1 to 20 ⁇ m.
- the volume ratio of the ceramic fiber in the raw material for forming the inorganic porous layer (volume ratio of the ceramic fiber in the material constituting the inorganic porous layer) may be 5% by volume or more and 25% by volume or less.
- the shrinkage of the ceramic particles in the inorganic porous layer can be sufficiently suppressed in the manufacturing process (firing step) of the inorganic porous layer.
- the volume ratio of the ceramic fibers in the raw material is set. It can be divided and heat transfer to the metal tube can be suitably suppressed.
- the ceramic fiber can also be confirmed by observing the cross section of the inorganic porous layer by SEM.
- the ceramic fibers are substantially circular in the SEM image.
- the ceramic fiber when the material of the ceramic fiber is different from other materials constituting the inorganic porous layer, the ceramic fiber can be discriminated (confirmed) by performing EDS analysis.
- the ratio (volume ratio) of the ceramic fiber in the inorganic porous layer should be measured by image processing the result of EDS analysis. You can also.
- alumina Al 2 O 3
- spinel MgAl 2 O 4
- titania TiO 2
- zirconia ZrO 2
- magnesia MgO
- mullite Al 6 O 13 Si 2
- cordierite MgO ⁇ Al 2 O 3 ⁇ SiO 2
- yttria Y 2 O 3
- steatite MgO ⁇ SiO 2
- forsterite 2MgO ⁇ SiO 2
- strontium A material similar to the material of the plate-shaped ceramic particles described above, such as titanate (SrTiO 3), can be used.
- the inorganic porous layer may contain one or more kinds of ceramic fibers formed of the above materials.
- the content of aggregates and reinforcing materials (ceramic fibers, plate-shaped ceramic particles, etc., hereinafter simply referred to as aggregates) in the raw materials for forming the inorganic porous layer is 15% by mass or more and 55% by mass or less. May be.
- the content of the aggregate in the raw material is 15% by mass or more, the shrinkage of the inorganic porous layer in the firing step can be sufficiently suppressed.
- the content of the aggregate in the raw material is 55% by mass or less, the aggregates are satisfactorily bonded to each other by the ceramic particles.
- the content of the aggregate in the raw material may be 20% by mass or more, 30% by mass or more, 50% by mass or more, or 53% by mass or more.
- the content of the aggregate in the raw material may be 53% by mass or less, 50% by mass or less, 30% by mass or less, or 20% by mass or less.
- both the ceramic fiber and the plate-shaped ceramic particle can function as an aggregate and a reinforcing material in the inorganic porous layer.
- the inorganic porous layer is used.
- the content of the ceramic fiber in the raw material when forming the layer may be at least 5% by mass or more.
- the content of the ceramic fiber in the raw material may be 10% by mass or more, 20% by mass or more, 30% by mass or more, or 40% by mass or more.
- the content of the ceramic fiber in the raw material may be 50% by mass or less, 40% by mass or less, 30% by mass or less, 20% by mass or less, and 10% by mass. It may be less than or equal to%.
- the ratio of the plate-shaped ceramic particles to the entire aggregate may be 70% by mass or less. That is, in terms of mass ratio, at least 30% by mass or more of the aggregate may be ceramic fibers.
- the ratio of the plate-shaped ceramic particles to the entire aggregate may be 67% by mass or less, 64% by mass or less, 63% by mass or less, 60% by mass or less, and 50. It may be mass% or less.
- the plate-shaped ceramic particles are not always essential as an aggregate.
- the ratio of the plate-shaped ceramic particles to the entire aggregate may be 40% by mass or more, 50% by mass or more, 60% by mass or more, and 62% by mass or more. , 63% by mass or more, and may be 65% by mass or more.
- the content of the plate-shaped ceramic particles in the raw material for forming the inorganic porous layer may be 5% by mass or more and 35% by mass or less.
- 5% by mass or more of plate-shaped ceramic particles as the raw material of the inorganic porous layer it is possible to sufficiently suppress the shrinkage of the ceramic particles in the inorganic porous layer in the manufacturing process (firing step) of the inorganic porous layer. can.
- the content of the plate-shaped ceramic particles in the raw material to 35% by mass or less (that is, the proportion of the plate-shaped ceramic particles in the inorganic porous layer is 35% by mass or less)
- the transfer in the inorganic porous layer is performed.
- the heat path can be divided, and heat transfer to the metal tube can be suitably suppressed.
- the content of the plate-shaped ceramic particles in the raw material may be 5% by mass or more, 10% by mass or more, 20% by mass or more, 30% by mass or more, and 33% by mass. It may be% or more.
- the content of the plate-shaped ceramic particles in the raw material may be 35% by mass or less, 33% by mass or less, 30% by mass or less, or 20% by mass or less. It may be 10% by mass or less.
- the SiO 2 contained in the inorganic porous layer may be 25% by mass or less.
- the formation of an amorphous layer in the inorganic porous layer is suppressed, and the heat resistance (durability) of the inorganic porous layer is improved.
- a raw material in which a binder, a pore-forming material, and a solvent are mixed may be used in addition to ceramic particles, plate-shaped ceramic particles, and ceramic fibers.
- a binder an inorganic binder may be used.
- the inorganic binder include alumina sol, silica sol, titania sol, zirconia sol and the like. These inorganic binders can improve the strength of the inorganic porous layer after firing.
- a polymer-based pore-forming material, carbon-based powder, or the like may be used as the pore-forming material.
- the pore-forming material may have various shapes depending on the purpose, and may be, for example, spherical, plate-shaped, fibrous, or the like. By selecting the addition amount, size, shape, etc. of the pore-forming material, the porosity and pore size of the inorganic porous layer can be adjusted.
- the solvent may be any solvent as long as the viscosity of the raw material can be adjusted without affecting other raw materials, and for example, water, ethanol, isopropyl alcohol (IPA) or the like can be used.
- the above-mentioned inorganic binder is also a constituent material of the inorganic porous layer. Therefore, when alumina sol, titania sol, etc. are used to form the inorganic porous layer, the inorganic porous layer contains 15% by mass or more of the alumina component and 45% by mass or more of the titania component in the entire constituent material including the inorganic binder. It may be included.
- the composition and raw material of the inorganic porous layer are adjusted according to the type of the metal tube.
- the exhaust pipe disclosed in the present specification is not particularly limited, but as the metal pipe, stainless steel such as SUS430, SUS429, SUS444, iron, cast iron, copper, Hastelloy, Inconel, Kovar, nickel alloy and the like can be used.
- the composition and raw material of the inorganic porous layer may be adjusted according to the coefficient of thermal expansion of the metal tube used. Specifically, when the coefficient of thermal expansion of the inorganic porous layer is ⁇ 1 and the coefficient of thermal expansion of the metal tube is ⁇ 2, the following equation 1 may be adjusted to be satisfied.
- the coefficient of thermal expansion ⁇ 1 is 6 ⁇ 10 -6 / K ⁇ 1 ⁇ 14 ⁇ 10 -6 / K, and more preferably the coefficient of thermal expansion ⁇ 1 is 6 ⁇ 10 -6.
- the composition and raw materials of the inorganic porous layer may be adjusted so that / K ⁇ 1 ⁇ 11 ⁇ 10-6 / K.
- the coefficient of thermal expansion ⁇ 1 is 8.5 ⁇ 10 -6 / K ⁇ 1 ⁇ 20 ⁇ 10 -6 / K, and more preferably, the coefficient of thermal expansion ⁇ 1 is 8.5.
- composition and raw materials of the inorganic porous layer may be adjusted so that ⁇ 10-6 / K ⁇ 1 ⁇ 18 ⁇ 10-6 / K.
- the value of " ⁇ 1 / ⁇ 2" may be 0.55 or more, 0.6 or more, 0.65 or more, 0.75 or more, and 0.8. It may be the above. Further, the value of " ⁇ 1 / ⁇ 2" may be 1.15 or less, 1.1 or less, 1.05 or less, or 1.0 or less. Equation 1: 0.5 ⁇ 1 / ⁇ 2 ⁇ 1.2
- the above raw material may be applied to the inner surface of the metal pipe, dried and fired to form an inorganic porous layer on the inner surface of the metal pipe.
- a method for applying the raw material dip coating, spin coating, aerosol deposition (AD) method, brush coating, trowel coating, mold cast molding and the like can be used. If the target inorganic porous layer is thick, or if the inorganic porous layer has a multi-layer structure, the application of the raw material and the drying of the raw material are repeated multiple times to adjust the thickness to the target or the multi-layer structure. You may.
- the above coating method can also be applied as a coating method for forming a coating layer, which will be described later.
- a coating layer may be provided on the surface of the inorganic porous layer (the surface opposite to the metal pipe side). That is, the inorganic porous layer may be sandwiched between the metal tube and the coating layer.
- the coating layer may be provided on the entire surface of the surface of the inorganic porous layer, or may be provided on a part of the surface of the inorganic porous layer.
- the material of the coating layer may be a porous or dense ceramic.
- the porous ceramic used in the coating layer include zirconia (ZrO 2 ), partially stabilized zirconia, stabilized zirconia and the like.
- yttria-stabilized zirconia ZrO 2- Y 2 O 3 : YSZ
- a metal oxide obtained by adding Gd 2 O 3 , Yb 2 O 3 , Er 2 O 3, etc.
- the dense ceramic used in the coating layer examples include alumina, silica, zirconia and the like. Further, by removing the ceramic fibers and the plate-shaped ceramic particles from the constituent materials of the above-mentioned inorganic porous layer, the porosity becomes low (dense), so that it may be used as a coating layer.
- the porous or dense ceramic as the coating layer, the inorganic porous layer can be reinforced and the inorganic porous layer can be prevented from peeling off from the surface of the metal tube.
- a dense ceramic is used as the coating layer, for example, it is possible to suppress the permeation of high-temperature gas through the inorganic porous layer and the retention of exhaust gas in the inorganic porous layer. As a result, the effect of suppressing the heat transfer of the exhaust gas to the metal pipe can be expected.
- the exhaust pipe 10 will be described with reference to FIGS. 1 to 3.
- the exhaust pipe 10 is provided with an inorganic porous layer 4 on the inner surface of a metal pipe 2 made of SUS430.
- the inorganic porous layer 4 is joined to the inner surface of the metal tube 2 (see FIGS. 1 and 2).
- the exhaust pipe 10 was manufactured by immersing the metal pipe 2 in the raw material slurry, drying and firing the metal pipe 2 with the outer surface of the metal pipe 2 masked.
- the raw material slurry was alumina fiber (average fiber length 140 ⁇ m), plate-shaped alumina particles (average particle diameter 6 ⁇ m), rutile-type titania particles (average particle diameter 0.25 ⁇ m), and alumina sol (alumina amount 1.1% by mass).
- Acrylic resin (average particle size 8 ⁇ m) and ethanol were mixed to prepare.
- the raw material slurry was adjusted so that the viscosity was 2000 mPa ⁇ s.
- the metal tube 2 After immersing the metal tube 2 in the raw material slurry and applying the raw material to the inner surface of the metal tube 2, the metal tube 2 was put into a dryer and dried at 200 ° C. (atmospheric atmosphere) for 1 hour. As a result, an inorganic porous layer of about 300 ⁇ m was formed on the inner surface of the metal tube 2. Then, the step of immersing the metal tube 2 in the raw material slurry and drying it was repeated three times to form a 1.2 mm inorganic porous layer on the inner surface of the metal tube 2. Then, the metal pipe 2 was placed in an electric furnace and fired at 800 ° C. in an atmospheric atmosphere to prepare an exhaust pipe 10.
- the inorganic porous layer 4 was formed on the entire inner surface of the metal tube 2 (see FIG. 3).
- the porosity of the inorganic porous layer 4 was 61% by volume, and the coefficient of thermal expansion was 7 ⁇ 10 -6 K- 1 .
- the titania particles were interposed between the aggregates and joined the aggregates in the exhaust pipe 10. It was also confirmed that the titania particles were interposed between the inner surface of the metal tube 2 and the aggregate (alumina fibers and plate-like alumina particles), and joined the inner surface of the metal tube 2 and the aggregate.
- the inorganic porous layer prepares a raw material slurry in which alumina fibers, plate-like alumina particles, rutile-type titania particles, alumina sol, acrylic resin and ethanol are mixed, and the metal is immersed in the raw material slurry and then dried. And fired to create.
- the ratio of alumina fibers, plate-shaped alumina particles and titania particles, and the ratio of rutile-type titania particles to the total mass of titania particles are changed, and the alumina fibers are replaced with mullite fibers and the plate-shaped alumina particles are used.
- the state of the inorganic porous layer after firing and the state of the inorganic porous layer after the heating vibration test were confirmed.
- the amount of ceramic fibers (alumina fiber,glasse fiber), plate-shaped ceramic particles (plate-shaped alumina particles, plate-shaped mica), titania particles and zirconia particles, and the rutile type in the total mass of titania particles.
- the ratio of the titania particles was changed as shown in FIGS. % (1.1% by mass of alumina contained in the alumina sol) and 40% by mass of the acrylic resin were added, and the slurry viscosity was adjusted with ethanol to prepare a raw material slurry.
- the reduced amount of rutile-type titania particles was supplemented with anatase-type titania particles.
- the sample 9 does not use the plate-shaped ceramic particles, and the samples 1 to 11, 14, 16 and 17 do not use the zirconia particles.
- the raw material slurry is applied to SUS430 (SUS plate, SUS tube), and for samples 13 and 14, the raw material slurry is applied to copper (copper plate, copper tube), and the atmosphere atmosphere 200. After drying at ° C. for 1 hour, it was calcined at an air atmosphere of 800 ° C. for 3 hours.
- the number of times the raw material slurry was applied (the number of times the metal plate and the metal tube were immersed) in each sample was adjusted so that an inorganic porous layer of about 1.2 mm was formed on the metal surface (inner surface in the case of a metal tube).
- the difference in the amount of alumina component (ceramic fiber, plate-shaped ceramic particles) and titania component, and the ratio of various titania crystal phases (rutyl-type titania, anatase-type titania) to the total mass of titania particles is fired.
- the heat insulating property of the inorganic porous layer has not been evaluated.
- the appearance of the sample after firing was evaluated.
- the appearance was evaluated with a sample in which an inorganic porous layer was formed on a metal plate.
- the presence or absence of cracks and peeling was visually observed.
- FIG. 4 " ⁇ ” is attached to the sample in which crack and peeling did not occur, " ⁇ ” is attached to the sample in which one of crack and peeling occurred, and " ⁇ ” was attached to the sample in which both crack and peeling occurred.
- "X" is attached.
- a bulk body was formed using the above-mentioned raw material slurry, and then the bulk body was calcined at 800 ° C. to prepare a sample for measuring the ratio (mass%) of the alumina component and the titania component.
- the amounts of aluminum and titanium were measured using an ICP emission spectrometer (PS3520UV-DD, manufactured by Hitachi High-Tech Science Co., Ltd.).
- FIGS. 4 and 5 show the results of converting the amounts of aluminum and titanium into oxides (Al 2 O 3 , TiO 2).
- Porosity was measured for Samples 1 to 17.
- the bulk body was used for measuring the porosity.
- the crystal structure of samples 1 to 17 was analyzed.
- the sample for analyzing the crystal structure was a sample obtained by pulverizing the bulk body into powder. Specifically, X-ray diffraction measurement was performed using an XRD device (D8-ADVANCE manufactured by Bruker-AXS), and the obtained diffraction putter was analyzed by the Rietveld method, and the ratio of the rutile type crystal phase to the titania crystal phase. was calculated.
- FIGS. 4 and 5 show the ratio of the rutile-type crystal phase to the titania crystal phase. In Sample 5, no rutile-type titania crystal phase was confirmed, and all were anatase-type crystal phases.
- a heating vibration test was performed on the samples 1 to 17.
- the heating thermal vibration test was performed on a sample in which an inorganic porous layer was formed on the inner surface of a metal tube. Specifically, the outer surface of a pipe (made of SUS430, made of copper) having an inner diameter of ⁇ 55 mm, an outer diameter of ⁇ 62 mm (thickness 3.5 mm), and a length of 80 mm is immersed in the raw material slurry with the outer surface masked, and the inorganic porous layer is placed on the inner wall of the pipe. was applied to. Then, each sample was prepared by drying at 200 ° C. and calcining at 800 ° C.
- the sample was attached to the heating vibration test device, and the combustion gas of propane was circulated in the pipe for 5 minutes from the heating vibration test device, and then the normal temperature air gas was circulated for 5 minutes.
- the combustion gas was adjusted so that the gas temperature at the end face on the inflow side of the pipe was 900 ° C. at the maximum and the gas flow rate was 2.0 Nm 3 / min.
- vibration in the longitudinal direction (longitudinal direction) was applied to the pipe.
- the vibration conditions were 100 Hz and 30 G, and vibration was applied for 50 hours.
- the test was conducted under these conditions, and the rate of change in weight (rate of weight loss) before and after the test was measured.
- rate of change in weight rate of weight loss
- the coefficient of thermal expansion of the inorganic porous layer and the metal (metal plate) was measured.
- the sample for measuring the coefficient of thermal expansion of the inorganic porous layer was prepared by molding the above-mentioned raw material slurry into a bulk body having a size of 4 mm ⁇ 3 mm ⁇ 20 mm and then firing the bulk body at 800 ° C.
- As the sample for measuring the coefficient of thermal expansion of the metal a sample having a size of 4 mm ⁇ 3 mm ⁇ 20 mm was used.
- the measurement sample was measured using a thermal expansion meter in accordance with JIS R1618 (measurement method of thermal expansion by thermomechanical analysis of fine ceramics).
- FIG. 5 shows the result of the coefficient of thermal expansion.
- the thermal conductivity of the inorganic porous layer and the metal was measured. Thermal conductivity was also measured using separate bulk bodies for the inorganic porous layer and the metal plate. The thermal conductivity was calculated by multiplying the thermal diffusivity, the specific heat capacity and the bulk density. For the heat diffusion rate, a laser flash method heat constant measuring device is used, and for the specific heat capacity, a DSC (differential scanning calorimetry) is used. Method) was measured at room temperature. For the bulk density of the metal plate, the weight of a bulk body having a diameter of 10 mm and a thickness of 1 mm was measured, and the value obtained by dividing the weight by the volume was taken as the bulk density (unit: g / cm 3 ).
- the bulk density (unit: g / cm 3 ) of the inorganic porous layer was calculated from the following formula (3).
- the thermal diffusivity is obtained by molding the above-mentioned raw material slurry into a bulk body having a diameter of 10 mm ⁇ 1 mm
- the specific heat capacity is obtained by molding the above-mentioned raw material slurry into a bulk body having a diameter of 5 mm ⁇ a thickness of 1 mm, and then each bulk body is 800.
- the proportion of the alumina component in the sample 15 is less than 15% by mass, it is presumed that the bonding force between the ceramics (particles, fibers) is reduced and cracks are generated in the inorganic porous layer. Further, since the proportion of the titania component in the sample 16 is less than 45% by mass, it is presumed that the bonding force between the ceramics is lowered and cracks are generated in the inorganic porous layer. Further, in the sample 16, the content of the titania component (titania particles) having a high coefficient of thermal expansion is low, and the ratio of the coefficient of thermal expansion to the metal ( ⁇ 1 / ⁇ 2) is small (less than 0.5).
- the inorganic porous layer was separated from the metal based on the difference in thermal expansion. From the above, regardless of the type of ceramic fiber (alumina fiber, mullite fiber) and the type of plate-shaped ceramic particles (plate-shaped alumina particle, plate-shaped mica), 15% by mass or more of alumina component and 45% by mass or more of titania component. It was confirmed that the inorganic porous layer containing the above was less likely to cause deterioration such as cracks and peeling after firing.
- Sample 5 does not contain a rutile-type crystal phase in the titania component (a binder that binds alumina fibers and plate-like alumina particles) (it is an anatase-type crystal phase), and is titania by circulating high-temperature LP gas. It is presumed that the crystal undergoes a phase transition and the volume of the titania component (binding material) changes. Further, in Samples 6 and 9, the weight of the inorganic porous layer after the heating vibration test was significantly reduced, although it was a passing level, as compared with the other samples 1 to 4,7,8,10 to 14,17.
- the rutile-type crystal phase constituting the titania component is 50% by mass or less (40% by mass), and the proportion of the anatase-type crystal phase is large. Therefore, it is presumed that the titania crystals undergo a phase transition and the volume of the titania component (binding material) changes due to the circulation of high-temperature LP gas. As a result, it is presumed that a part of the inorganic porous layer was damaged and the mass was reduced.
- the rutile-type titania crystal phase is 100% by mass, but since it does not contain plate-like alumina particles, the inorganic porous layer is not sufficiently reinforced, and when a high-temperature LP gas is circulated, it is circulated. It is presumed that a part of the inorganic porous layer was damaged. From the above, it was confirmed that if the rutile-type crystal phase is contained in the titania component constituting the inorganic porous layer, an inorganic porous layer having high resistance to vibration and thermal shock can be obtained. In particular, it was confirmed that the inorganic porous layer in which the rutile-type crystal phase accounts for 50% by mass or more of the titania component is most suitable as the inorganic porous layer used for the exhaust pipe.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Organic Chemistry (AREA)
- General Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Structural Engineering (AREA)
- Combustion & Propulsion (AREA)
- Manufacturing & Machinery (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Inorganic Chemistry (AREA)
- Metallurgy (AREA)
- Porous Artificial Stone Or Porous Ceramic Products (AREA)
Abstract
排気管は、金属管と、金属管の内面の排気ガスが通過する部位に設けられている無機多孔質層を備えている。この排気管では、無機多孔質層は、セラミック繊維を含み、15質量%以上のアルミナ成分と45質量%以上のチタニア成分によって構成されており、チタニア成分はルチル型結晶相を含んでいる。
Description
本出願は、2020年7月13日に出願された日本国特許出願第2020-120260号に基づく優先権を主張する。その出願の全ての内容は、この明細書中に参照により援用されている。本明細書は、排気管に関する技術を開示する。
特開2018-031346号公報(以下、特許文献1と称する)に、金属製の内管と金属製の外管の間に無機多孔質層(断熱材)が配置された内燃機関の排気管が開示されている。特許文献1は、内管と外管の間に無機多孔質層を設けることにより、内管と外管の間を断熱し、排気管の下流に設けられている触媒に流入する排気ガスの温度低下を抑制している。触媒に流入する排気ガスの温度低下を抑制することにより、触媒の暖機が早期に完了する。
特許文献1のように、二重管の間に無機多孔質層を配置する場合、排気ガスは無機多孔質層に直接接触しない。そのため、無機多孔質層は、専ら断熱性能を有していればよい。しかしながら、二重管の内管の内側、あるいは、単管の内側に無機多孔質層を設ける場合、排気ガスが無機多孔質層に直接接触し、無機多孔質層が高温に曝される。よって、排気ガスが通過する部位に無機多孔質層を設ける場合、無機多孔質層の耐熱衝撃性を向上させることが必要である。本明細書では、金属管の排気ガスが通過する部位に無機多孔質層が設けられている新規な排気管を提供することを目的とする。
本明細書で開示する排気管は、金属管と、金属管の内面の排気ガスが通過する部位に設けられている無機多孔質層を備えていてよい。この排気管では、無機多孔質層は、セラミック繊維を含み、15質量%以上のアルミナ成分と45質量%以上のチタニア成分によって構成されており、チタニア成分は、ルチル型結晶相を含んでいてよい。
本明細書で開示する排気管は、金属管と、金属管の内面の排気ガスが通過する部位に設けられている無機多孔質層を備えている。また、無機多孔質層は、セラミック繊維を含んでいてよい。セラミック繊維は、金属管と無機多孔質層の熱膨張率差の影響を吸収することができる。具体的には、無機多孔質層が金属管の変形(熱膨張,熱収縮)に追従して変形することができるので、金属管から無機多孔質層が剥離することを防止することができる。すなわち、金属管と無機多孔質層の密着性が向上する。また、上記排気管は、無機多孔質層によって、排気ガスが金属管に接することを抑制し、金属管が劣化することを抑制することもできる。また、無機多孔質層は、15質量%以上のアルミナ成分と45質量%以上のチタニア成分によって構成されているので、無機多孔質層自体の融点が高く、排気ガスの熱によって形状が変化することも抑制できる。
無機多孔質層を構成するチタニア成分には、ルチル型結晶相が含まれていてよい。なお、チタニア成分には、ルチル型結晶相の他、アナターゼ型結晶相、ブルッカイト型結晶相、非晶質相が含まれていてもよい。ルチル型のチタニアは、他の結晶相及び非晶質相と比較して、高温環境下において安定である。具体的には、ルチル型のチタニアは、高温に曝されても相転移が起こらない。そのため、ルチル型のチタニアを含む無機多孔質層は、相転移に伴う体積変化が起こりにくく、内部応力が生じにくい。その結果、高温の排気ガスが無機多孔質層に直接接触しても、無機多孔質層の劣化が抑制される。すなわち、無機多孔質層を構成するチタニア成分にルチル型結晶相が含まれることにより、無機多孔質層の耐熱衝撃性が向上する。なお、アナターゼ型結晶相及びブルッカイト型結晶相は、高温環境下においてルチル型結晶相に相転移する。
なお、チタニア成分は、ルチル型結晶相を主体としていてよい。すなわち、ルチル型結晶相が、チタニア成分の50質量%以上を占めていてよい。上記したように、ルチル型結晶相は、高温環境下において安定である。そのため、ルチル型結晶相がチタニア成分の50質量%以上を占めていれば、無機多孔質層の耐熱衝撃性が顕著に向上する。なお、チタニア成分に占めるルチル型結晶相の割合は、60質量%以上であってよく、70質量%以上であってよく、80質量%以上であってよく、90質量%以上であってよく、チタニア成分の全てがルチル型結晶相であってもよい。
無機多孔質層の熱膨張係数をα1とし、金属管の熱膨張係数をα2としたときに、下記式(1)を満足していてよい。無機多孔質層が金属管から剥離する現象を、より確実に防止することができる。
式1:0.5<α1/α2<1.2
式1:0.5<α1/α2<1.2
無機多孔質層に扁平板状の板状セラミック粒子が含まれていてよい。板状セラミック粒子を用いることにより、セラミック繊維の一部を板状セラミック粒子に置換することができる。典型的に、板状セラミック粒子の長さ(長手方向サイズ)は、セラミック繊維の長さより短い。そのため、板状セラミック粒子を用いることにより、無機多孔質層内の伝熱経路が分断され、無機多孔質層内の熱伝達が起こりにくくなる。その結果、無機多孔質層の断熱性能がさらに向上する。
無機多孔質層に、0.1μm以上10μm以下の粒状粒子が含まれていてよい。無機多孔質層を成形(焼成)する際、セラミック繊維同士が粒状粒子を介して結合され、高強度の無機多孔質層が得られる。また、無機多孔質層の厚みは、1mm以上であってよい。これにより、排気管の断熱性を十分に発揮することができる。なお、上記排気管は、無機多孔質層がセラミック繊維を含んでいるので、1mm以上の無機多孔質層を実現することができる。すなわち、無機多孔質層を成形する過程(例えば、焼成工程)において収縮が起こり難いセラミック繊維を含むので、無機多孔質層を1mm以上に成形することができる。例えば、無機多孔質層がセラミック繊維を含んでいない場合、成形する過程で無機多孔質層が収縮し、クラック等が発生する、そのため、無機多孔質層がセラミック繊維を含んでいない場合、無機多孔質層を1mm以上という厚膜に形成することが困難である。
上記したように、無機多孔質層は、15質量%以上55質量%以下のアルミナ(Al2O3)成分と、45質量%以上85質量%以下のチタニア(TiO2)成分によって構成されている。なお、無機多孔質層に含まれるアルミナ成分は、25質量%以上であってよく、30質量%以上であってよく、40質量%以上であってもよい。
金属管と無機多孔質層は、熱伝導率の差が大きいことが好ましい。具体的には、金属管の熱伝導率は、無機多孔質層の熱伝導率の100倍以上であってよい。なお、金属管の熱伝導率は、無機多孔質層の熱伝導率の150倍以上であってよく、無機多孔質層の熱伝導率の200倍以上であってよく、無機多孔質層の熱伝導率の250倍以上であってよく、無機多孔質層の熱伝導率の300倍以上であってもよい。
金属管の熱伝導率は、10W/mK以上400W/mK以下であってよい。なお、金属管の熱伝導率は、25W/mK以上であってよく、50W/mK以上であってよく、100W/mK以上であってよく、150W/mK以上であってよく、200W/mK以上であってよく、250W/mK以上であってよく、300W/mK以上であってよく、380W/mK以上であってもよい。また、金属管の熱伝導率は、350W/mK以下であってよく、300W/mK以下であってよく、250W/mK以下であってよく、200W/mK以下であってよく、150W/mK以下であってもよい。
無機多孔質層の熱伝導率は、0.05W/mK以上3W/mK以下であってよい。なお、無機多孔質層の熱伝導率は、0.1W/mK以上であってよく、0.2W/mK以上であってよく、0.3W/mK以上であってよく、0.5W/mK以上であってよく、0.7W/mK以上であってよく、1W/mK以上であってよく、1.5W/mK以上であってよく、2W/mK以上であってもよい。また、無機多孔質層の熱伝導率は、2.5W/mK以下であってよく、2.0W/mK以下であってよく、1.5W/mK以下であってよく、1W/mK以下であってよく、0.5W/mK以下であってよく、0.3W/mK以下であってよく、0.25W/mK以下であってもよい。
金属管は、単管であってもよいし、多重管(例えば二重管)であってもよい。金属管は、直線状であってもよく、全体(または一部)が曲線状であってもよく、中間部分がテーパー状であってもよく、また、分岐管であってもよい。無機多孔質層は、単管の場合は金属管の内面、多重管の場合は最も内側に配置されている金属管の内面に設けられていてよい。なお、無機多孔質層は、金属管内面の全面を被覆していてもよいし、金属管内面の一部を被覆していてもよい。例えば、無機多孔質層は、金属管の端部(一端または両端)を除く部分を被覆していてよい。
また、無機多孔質層は、厚み方向において、均一の材料で構成されていてよい。すなわち、無機多孔質層は単層であってよい。また、無機多孔質層は、厚み方向において、組成の異なる複数の層で構成されていてもよい。すなわち、無機多孔質層は、複数の層が積層した多層構造であってよい。あるいは、無機多孔質層は、厚み方向において、組成が除々に変化する傾斜構造であってもよい。無機多孔質層が単層の場合、排気管の製造(金属管の内面に無機多孔質層を成形する工程)を容易に行うことができる。無機多孔質層が多層又は傾斜構造の場合、厚み方向において、無機多孔質層の特性を変化させることができる。例えば、無機多孔質層の表層において、チタニア成分に占めるルチル型結晶相の割合を、他の部分より大きくすることができる。無機多孔質層の構造(単層、多層、傾斜構造)については、排気管の使用目的に応じて適宜選択することができる。
無機多孔質層の気孔率は、45体積%以上90体積%以下であってよい。気孔率が45体積%以上であれば、断熱性を十分に発揮し得る。また、気孔率が90体積%以下であれば、十分な強度を確保することができる。なお、無機多孔質層の気孔率は、55体積%以上であってよく、60体積%以上であってよく、65体積%以上であってもよい。さらに、無機多孔質層の気孔率は、85体積%以下であってよく、80体積%以下であってよく、70体積%以下であってよく、65体積%以下であってよく、60体積%以下であってもよい。また、無機多孔質層が多層構造又は傾斜構造の場合、無機多孔質層の気孔率は、全体として45体積%以上90体積%以下であればよく、厚み方向で気孔率が異なっていてもよい。この場合、部分的に、気孔率が45体積%未満の部分、あるいは、気孔率が90体積%超の部分が存在していてよい。
無機多孔質層の厚みは、要求性能に依るが、1mm以上であってよい。無機多孔質層の厚みが1mm以上であれば、断熱性を十分に発揮し得る。なお、セラミック繊維が用いられていない無機多孔質層の場合、製造過程(例えば焼成工程)において収縮するため、厚みを1mm以上に維持することが困難である。本明細書で開示する無機多孔質層は、セラミック繊維を含んでいるので、製造過程における収縮が抑制され、1mm以上の厚みを維持することができる。なお、無機多孔質層の厚みが厚すぎると、コスト(製造コスト、材料コスト)に見合う断熱性の向上が得られにくくなる。そのため、特に限定されないが、無機多孔質層の厚みは、30mm以下であってよく、20mm以下であってよく、15mm以下であってよく、10mm以下であってよく、5mm以下であってよい。
無機多孔質層は、セラミック粒子(粒状粒子)、板状セラミック粒子、セラミック繊維のうちの1以上の材料により構成されている。なお、セラミック粒子、板状セラミック粒子及びセラミック繊維は、構成成分として、アルミナ、及び/又は、チタニアを含んでいてよい。換言すると、アルミナ、及び/又は、チタニアによって、セラミック粒子、板状セラミック粒子、セラミック繊維が形成されていてよい。すなわち、無機多孔質層は、構成材料(構成物質)全体で、15質量%以上のアルミナ成分と45質量%以上のチタニア成分を含んでいればよい。但し、無機多孔質層は、構成成分は任意(アルミナ成分、チタニア成分を含んでいてもよいし、含んでいなくてもよい)であるが、少なくともセラミック繊維を含んでいる。
セラミック粒子は、板状セラミック粒子,セラミック繊維等の無機多孔質層の骨格をなす骨材同士を接合する接合材として用いられてよい。セラミック粒子は、0.1μm以上10μm以下の粒状粒子であってよい。なお、セラミック粒子は、製造過程(例えば焼成工程)において、焼結等により粒径が大きくなってもよい。すなわち、無機多孔質層を製造する原料として、セラミック粒子は、0.1μm以上10μm以下(焼成前の平均粒径)の粒状粒子であってよい。なお、セラミック粒子は、0.5μm以上であってよく、5μm以下であってもよい。セラミック粒子の材料として、例えば金属酸化物を利用してよい。金属酸化物の一例として、アルミナ(Al2O3)、スピネル(MgAl2O4)、チタニア(TiO2)、ジルコニア(ZrO2)、マグネシア(MgO)、ムライト(Al6O13Si2)、コージェライト(MgO・Al2O3・SiO2)、イットリア(Y2O3)、ステアタイト(MgO・SiO2)、フォルステライト(2MgO・SiO2)、ランタンアルミネート(LaAlO3)、ストロンチウムチタネート(SrTiO3)等が挙げられる。これらの金属酸化物は、高い耐蝕性を有し、排気管の保護層として好適に適用することができる。なお、セラミック粒子がチタニア粒子を含む場合、チタニア粒子がルチル型結晶相を含むことにより、骨材同士を接合する接合材の耐熱衝撃性が向上し、無機多孔質層の劣化が抑制される。
板状セラミックは、無機多孔質層内において、骨材、補強材として機能し得る。すなわち、板状セラミックは、セラミック繊維と同様に、無機多孔質層の強度を向上させ、さらに、製造工程において無機多孔質層が収縮することを抑制する。なお、板状セラミック粒子を用いることにより、無機多孔質層内の伝熱経路を分断することができる。そのため、骨材としてセラミック繊維のみを用いる形態と比較して、断熱性を向上させることができる。
扁平板状の板状セラミック粒子は、表面形状(厚み方向から観察した形状)は特に限定されず、例えば、矩形等の多角形、略円形、曲線及び/又は直線で囲まれた不定形よく、断面を観察したときの長手方向サイズが5μm以上100μm以下であってよい。長手方向サイズが5μm以上であれば、セラミック粒子の過剰な焼結を抑制することができる。長手方向サイズが100μm以下であれば、上述したように無機多孔質層内の伝熱経路を分断する効果が得られ、高温環境で用いる排気管に好適に適用し得る。また、無機多孔質層に含まれる板状セラミック粒子は、断面をSEMで観察したときのアスペクト比が10以上60以下であってよい。なお、断面のアスペクト比が10以上60以下の板状セラミック粒子は、例えば、原料として断面のアスペクト比が60以上100以下の板状セラミック粒子を用いることにより、無機多孔質層の製造過程においてアスペクト比が小さくなり、結果として無機多孔質内に残存する。断面のアスペクト比が10以上であればセラミック粒子の焼結を良好に抑制することができる。また、断面のアスペクト比が10以上であれば、製造後(焼成後)に無機多孔質層が硬くなりすぎる(ヤング率が高くなりすぎる)ことを抑制することができる。その結果、内燃機関の始動直後の熱衝撃(低温状態の無機多孔質に高温の排気ガスが接触すること)によって無機多孔質層が破損する(クラック等が生じる)ことを抑制することができる。また、断面のアスペクト比が60以下であれば板状セラミック粒子自体の強度低下が抑制され、排気管の振動、あるいは、排気ガスのガス流によって無機多孔質層が破損することを抑制することができる。なお、板状セラミック粒子の材料として、上記したセラミック粒子の材料として用いられる金属酸化物に加え、タルク(Mg3Si4O10(OH)2)、マイカ、カオリン等の鉱物・粘土、ガラス等を用いることもできる。
セラミック繊維は、無機多孔質層内において、骨材、補強材として機能し得る。すなわち、セラミック繊維は、無機多孔質層の強度を向上させ、さらに、製造工程において無機多孔質層が収縮することを抑制する。セラミック繊維の長さは、50μm以上200μm以下であってよい。また、セラミック繊維の直径(平均径)は、1~20μmであってよい。無機多孔質層を形成する際の原料に占めるセラミック繊維の体積率(無機多孔質層を構成する材料に占めるセラミック繊維の体積率)は、5体積%以上25体積%以下であってよい。無機多孔質層の原料が5体積%以上のセラミック繊維を含むことにより、無機多孔質層の製造過程(焼成工程)において無機多孔質層内のセラミック粒子の収縮を十分に抑制することができる。また、原料中のセラミック繊維の体積率を25体積%以下(すなわち、無機多孔質層内のセラミック繊維の体積率が25体積%以下)とすることにより、無機多孔質層内の伝熱経路を分断することができ、金属管への伝熱を好適に抑制し得る。セラミック繊維も、無機多孔質層の断面をSEM観察することにより確認することができる。セラミック繊維は、SEM画像において略円形である。すなわち、SEM画像には、セラミック繊維の径方向断面が現れる。また、セラミック繊維の材料が無機多孔質層を構成する他の材料と異なる場合、EDS分析を行うことによってセラミック繊維を判別(確認)することもできる。なお、セラミック繊維の材料が無機多孔質層を構成する他の材料と異なる場合、EDS分析の結果を画像処理することにより、無機多孔質層内のセラミック繊維の割合(体積率)を測定することもできる。
なお、セラミック繊維の材料として、アルミナ(Al2O3)、スピネル(MgAl2O4)、チタニア(TiO2)、ジルコニア(ZrO2)、マグネシア(MgO)、ムライト(Al6O13Si2)、コージェライト(MgO・Al2O3・SiO2)、イットリア(Y2O3)、ステアタイト(MgO・SiO2)、フォルステライト(2MgO・SiO2)、ランタンアルミネート(LaAlO3)、ストロンチウムチタネート(SrTiO3)等、上述した板状セラミック粒子の材料と同様の材料を用いることができる。また、無機多孔質層内に、上記材料で形成された一種または複数種のセラミック繊維が含まれていてよい。
また、無機多孔質層を形成する際の原料に占める骨材、補強材(セラミック繊維,板状セラミック粒子等。以下、単に骨材と称する)の含有率は、15質量%以上55質量%以下であってよい。原料中の骨材の含有率が15質量%以上であれば、焼成工程における無機多孔質層の収縮を十分に抑制することができる。また、原料中の骨材の含有率が55質量%以下であれば、セラミック粒子によって骨材同士が良好に接合される。原料中の骨材の含有率は、20質量%以上であってよく、30質量%以上であってよく、50質量%以上であってよく、53質量%以上であってもよい。また、原料中の骨材の含有率は、53質量%以下であってよく、50質量%以下であってよく、30質量%以下であってよく、20質量%以下であってもよい。
上記したように、セラミック繊維及び板状セラミック粒子は、ともに無機多孔質層内において骨材、補強材として機能し得る。しかしながら、排気管の作製後(焼成後)に無機多孔質層が収縮することを確実に抑制するため、骨材としてセラミック繊維と板状セラミック粒子の双方を用いる場合であっても、無機多孔質層を形成する際の原料に占めるセラミック繊維の含有量は、少なくとも5質量%以上であってよい。なお、原料中のセラミック繊維の含有量は、10質量%以上であってよく、20質量%以上であってよく、30質量%以上であってよく、40質量%以上であってよい。また、原料中のセラミック繊維の含有量は、50質量%以下であってよく、40質量%以下であってよく、30質量%以下であってよく、20質量%以下であってよく、10質量%以下であってもよい。
骨材としてセラミック繊維と板状セラミック粒子の双方を用いる場合、骨材全体に占める板状セラミック粒子の割合は、70質量%以下であってよい。すなわち、質量比で、骨材の少なくとも30質量%以上がセラミック繊維であってよい。骨材全体に占める板状セラミック粒子の割合は、67質量%以下であってよく、64質量%以下であってよく、63質量%以下であってよく、60質量%以下であってよく、50質量%以下であってもよい。なお、板状セラミック粒子は必ずしも骨材として必須ではない。また、骨材全体に占める板状セラミック粒子の割合は、40質量%以上であってよく、50質量%以上であってよく、60質量%以上であってよく、62質量%以上であってよく、63質量%以上であってよく、65質量%以上であってもよい。
なお、無機多孔質層を形成する際の原料に占める板状セラミック粒子の含有量は、5質量%以上35質量%以下であってよい。無機多孔質層の原料が5質量%以上の板状セラミック粒子を含むことにより、無機多孔質層の製造過程(焼成工程)において無機多孔質層内のセラミック粒子の収縮を十分に抑制することができる。また、原料中の板状セラミック粒子の含有量を35質量%以下(すなわち、無機多孔質層内の板状セラミック粒子の割合を35質量%以下)とすることにより、無機多孔質層内の伝熱経路を分断することができ、金属管への伝熱を好適に抑制し得る。原料中の板状セラミック粒子の含有量は、5質量%以上であってよく、10質量%以上であってよく、20質量%以上であってよく、30質量%以上であってよく、33質量%以上であってよい。また、原料中の板状セラミック粒子の含有量は、35質量%以下であってよく、33質量%以下であってよく、30質量%以下であってよく、20質量%以下であってよく、10質量%以下であってもよい。
なお、無機多孔質層に含まれるSiO2は、25質量%以下であってよい。無機多孔質層内に非晶質層が形成されることが抑制され、無機多孔質層の耐熱性(耐久性)が向上する。
無機多孔質層を形成する際、セラミック粒子、板状セラミック粒子、セラミック繊維の他に、バインダ、造孔材、溶媒を混合した原料を用いてよい。バインダとして、無機バインダを使用してよい。無機バインダの一例として、アルミナゾル、シリカゾル、チタニアゾル、ジルコニアゾル等が挙げられる。これらの無機バインダは、焼成後の無機多孔質層の強度を向上させることができる。造孔材として、高分子系造孔材、カーボン系粉等を使用してよい。具体的には、アクリル樹脂、メラミン樹脂、ポリエチレン粒子、ポリスチレン粒子、カーボンブラック粉末、黒鉛粉末等が挙げられる。造孔材は、目的に応じて種々の形状であってよく、例えば、球状、板状、繊維状等であってよい。造孔材の添加量、サイズ、形状等を選択することにより、無機多孔質層の気孔率、気孔サイズを調整することができる。溶媒は、他の原料に影響を及ぼすことなく原料の粘度を調整可能なものであればよく、例えば、水、エタノール、イソプロピルアルコール(IPA)等を使用することができる。
なお、上記した無機バインダも無機多孔質層の構成材料である。そのため、無機多孔質層を形成する際にアルミナゾル、チタニアゾル等を用いる場合、無機多孔質層は、無機バインダを含む構成材料全体で、15質量%以上のアルミナ成分と45質量%以上のチタニア成分を含んでいればよい。
無機多孔質層の組成及び原料は、金属管の種類に応じて調整する。本明細書で開示する排気管では、特に限定されないが、金属管として、SUS430,SUS429,SUS444等のステンレス鋼、鉄、鋳鉄、銅、ハステロイ、インコネル、コバール、ニッケル合金等を用いることができる。無機多孔質層の組成及び原料は、用いる金属管の熱膨張係数に応じて調整してよい。具体的には、無機多孔質層の熱膨張係数をα1とし、金属管の熱膨張係数をα2としたときに、下記式1を満足するように調整してよい。例えば、金属管がSUS430の場合、熱膨張係数α1が6×10⁻⁶/K<α1<14×10-6/Kとなるように、より好ましくは、熱膨張係数α1が6×10-6/K<α1<11×10-6/Kとなるように、無機多孔質層の組成及び原料を調整してよい。また、金属管が銅の場合、熱膨張係数α1が8.5×10-6/K<α1<20×10-6/Kとなるように、より好ましくは、熱膨張係数α1が8.5×10-6/K<α1<18×10-6/Kとなるように、無機多孔質層の組成及び原料を調整してよい。なお、「α1/α2」の値は、0.55以上であってよく、0.6以上であってよく、0.65以上であってよく、0.75以上であってよく、0.8以上であってもよい。また、「α1/α2」の値は、1.15以下であってよく、1.1以下であってよく、1.05以下であってよく1.0以下であってもよい。
式1:0.5<α1/α2<1.2
式1:0.5<α1/α2<1.2
本明細書で開示する排気管では、金属管の内面に上記原料を塗布し、乾燥、焼成を経て金属管の内面に無機多孔質層を形成してよい。原料の塗布方法として、ディップコート、スピンコート、エアロゾルデポジション(AD)法、刷毛塗り、コテ塗り、モールドキャスト成形等を用いることができる。なお、目的とする無機多孔質層の厚みが厚い場合、あるいは、無機多孔質層が多層構造の場合、原料の塗布、原料の乾燥を複数回繰り返し、目的とする厚み、あるいは、多層構造に調整してもよい。上記塗布方法は、後述する被覆層を形成する塗布方法として適用することもできる。
また、本明細書で開示する排気管では、無機多孔質層の表面(金属管側とは反対側の面)に、被覆層が設けられていてもよい。すなわち、無機多孔質層が、金属管と被覆層によって挟まれていてよい。なお、被覆層は、無機多孔質層の表面の全面に設けられていてもよいし、無機多孔質層の表面の一部に設けられていてもよい。被覆層を設けることにより、無機多孔質層を保護(補強)することができる。
被覆層の材料は、多孔質または緻密質なセラミックであってよい。被覆層で用いられる多孔質セラミックの一例として、ジルコニア(ZrO2),部分安定化ジルコニア,安定化ジルコニア等が挙げられる。また、イットリア安定化ジルコニア(ZrO2-Y2O3:YSZ)、YSZにGd2O3、Yb2O3、Er2O3等を添加した金属酸化物、ZrO2-HfO2-Y2O3、ZrO2-Y2O3-La2O3、ZrO2-HfO2-Y2O3-La2O3、HfO2-Y2O3、CeO2-Y2O3、Gd2Zr2O7、Sm2Zr2O7、LaMnAl11O19、YTa3O9、Y0.7La0.3Ta3O9、Y1.08Ta2.76Zr0.24O9、Y2Ti2O7、LaTa3O9、Yb2Si2O7、Y2Si2O7、Ti3O5等が挙げられる。被覆層で用いられる緻密質なセラミックの一例として、アルミナ、シリカ、ジルコニアなどが挙げられる。また、上述した無機多孔質層の構成材料からセラミック繊維,板状セラミック粒子を除去することにより、低気孔率(緻密質)となるため、被覆層として用いてもよい。被覆層として多孔質または緻密質セラミックを用いることにより、無機多孔質層が補強され、無機多孔質層が金属管の表面から剥がれることを抑制することができる。なお、被覆層として緻密質なセラミックを用いると、例えば高温ガスが無機多孔質層を透過することを抑制したり、無機多孔質層内で排気ガスが滞留することを抑制することができる。その結果、排気ガスの熱が金属管に伝熱することを抑制する効果が期待できる。
図1から図3を参照し、排気管10について説明する。排気管10は、SUS430製の金属管2の内面に無機多孔質層4を備えている。無機多孔質層4は、金属管2の内面に接合している(図1及び図2を参照)。排気管10は、金属管2の外面をマスキングした状態で、金属管2を原料スラリーに浸漬し、乾燥、焼成を行って製造した。原料スラリーは、アルミナ繊維(平均繊維長140μm)と、板状アルミナ粒子(平均粒子径6μm)と、ルチル型チタニア粒子(平均粒子径0.25μm)と、アルミナゾル(アルミナ量1.1質量%)と、アクリル樹脂(平均粒子径8μm)と、エタノールを混合し、作成した。なお、原料スラリーは、粘度が2000mPa・sとなるように調整した。
金属管2を上記原料スラリーに浸漬して金属管2の内面に原料を塗布した後、金属管2を乾燥機に投入し、200℃(大気雰囲気)で1時間乾燥させた。これにより、金属管2の内面におよそ300μmの無機多孔質層が形成された。その後、金属管2を上記原料スラリーに浸漬して乾燥する工程を3回繰り返し、金属管2の内面に1.2mmの無機多孔質層を形成した。その後、金属管2を電気炉内に配置し、大気雰囲気で800℃で焼成し、排気管10を作成した。無機多孔質層4は、金属管2の内面全体に形成された(図3を参照)。得られた排気管10は、無機多孔質層4の気孔率が61体積%であり、熱膨張係数が7×10⁻⁶K-1であった。なお、図示は省略するが、排気管10では、チタニア粒子が、骨材同士の間に介在し、骨材同士を接合していることが確認された。また、チタニア粒子は、金属管2の内面と骨材(アルミナ繊維及び板状アルミナ粒子)の間に介在し、金属管2の内面と骨材を接合していることも確認された。
(実験例)
上記したように、無機多孔質層は、アルミナ繊維、板状アルミナ粒子、ルチル型チタニア粒子、アルミナゾル、アクリル樹脂及びエタノールを混合した原料スラリーを作成し、金属を原料スラリーに浸漬させた後、乾燥及び焼成を行い作成した。本実験例では、アルミナ繊維,板状アルミナ粒子及びチタニア粒子の割合、チタニア粒子の全質量に占めるルチル型チタニア粒子の割合を変化させ、また、アルミナ繊維をムライト繊維に代えるとともに板状アルミナ粒子を板状マイカに代え、焼成後の無機多孔質層の状態、加熱振動試験後の無機多孔質層の状態を確認した。
上記したように、無機多孔質層は、アルミナ繊維、板状アルミナ粒子、ルチル型チタニア粒子、アルミナゾル、アクリル樹脂及びエタノールを混合した原料スラリーを作成し、金属を原料スラリーに浸漬させた後、乾燥及び焼成を行い作成した。本実験例では、アルミナ繊維,板状アルミナ粒子及びチタニア粒子の割合、チタニア粒子の全質量に占めるルチル型チタニア粒子の割合を変化させ、また、アルミナ繊維をムライト繊維に代えるとともに板状アルミナ粒子を板状マイカに代え、焼成後の無機多孔質層の状態、加熱振動試験後の無機多孔質層の状態を確認した。
具体的には、セラミック繊維(アルミナ繊維,ムライト繊維)、板状セラミック粒子(板状アルミナ粒子,板状マイカ)、チタニア粒子及びジルコニア粒子の配合量、及び、チタニア粒子の全質量に占めるルチル型チタニア粒子の割合を図4,5に示すように変化させ、セラミック繊維、板状セラミック粒子、チタニア粒子及びジルコニア粒子の合計が100質量%になるように配合し、さらに、外掛けでアルミナゾル10質量%(アルミナゾルに含まれるアルミナ量1.1質量%)、アクリル樹脂40質量%を加え、エタノールでスラリー粘度を調整して原料スラリーを作成した。なお、ルチル型チタニア粒子を減らした分は、アナターゼ型チタニア粒子で補った。また、試料9は板状セラミック粒子を用いておらず、試料1~11,14,16及び17はジルコニア粒子を用いていない。その後、試料1~12,15~17についてはSUS430(SUS板、SUS管)に原料スラリーを塗布し、試料13及び14については銅(銅板、銅管)に原料スラリーを塗布し、大気雰囲気200℃で1時間乾燥させた後、大気雰囲気800℃で3時間焼成した。なお、金属表面(金属管の場合内面)に約1.2mmの無機多孔質層が形成されるように、各試料における原料スラリーの塗布回数(金属板及び金属管の浸漬回数)を調整した。
なお、本実験例は、アルミナ成分(セラミック繊維、板状セラミック粒子)及びチタニア成分の量、チタニア粒子の全質量に占める各種チタニア結晶相(ルチル型チタニア、アナターゼ型チタニア)の割合の相違が焼成後の無機多孔質層の外観に及ぼす影響(クラック、剥離等の有無)、および耐加熱振動性を確認することを目的とし、無機多孔質層の断熱性の評価は行っていない。
焼成後の試料について、外観の評価を行った。外観評価は、金属板上に無機多孔質層を形成した試料にて行った。外観評価は、目視にて、クラック及び剥離の発生の有無を観察した。図4に、クラック及び剥離等が発生しなかった試料に「〇」を付し、クラックと剥離の一方が発生した試料に「△」を付し、クラックと剥離の両方が発生した試料に「×」を付している。
試料1~17について、上記した原料スラリーを用いてバルク体を成形した後バルク体を800℃で焼成し、アルミナ成分とチタニア成分の割合(質量%)を測定するための試料を作製した。アルミナ及びチタニア成分は、ICP発光分析装置((株)日立ハイテクサイエンス製、PS3520UV-DD)を用いてアルミニウム及びチタン量を測定した。図4,5に、アルミニウム及びチタン量を酸化物換算(Al2O3、TiO2)した結果を示している。
試料1~17について、気孔率の測定を行った。気孔率の測定は、上記バルク体を利用した。気孔率は、水銀ポロシメーターを用いてJIS R1655(ファインセラミックスの水銀圧入法による成形体気孔径分布試験方法)に準拠して測定した全細孔容積(単位:cm3/g)と、ガス置換式密度測定計(マイクロメリティックス社製、アキュピック1330)により測定した見掛け密度(単位:g/cm3)を用いて、下記式(2)より算出した。
式2:気孔率[%]=全細孔容積/{(1/見掛け密度)+全細孔容積} ×100
式2:気孔率[%]=全細孔容積/{(1/見掛け密度)+全細孔容積} ×100
試料1~17について、結晶構造の解析を行った。結晶構造を解析するための試料は、上記バルク体を粉状に粉砕した試料で実施した。具体的には、XRD装置(Bruker-AXS製D8-ADVANCE)を用いてX線回折測定を行い、得られた回折パターをリートベルト法で解析し、チタニア結晶相に占めるルチル型結晶相の割合を算出した。図4,5に、チタニア結晶相に占めるルチル型結晶相の割合を示す。なお、試料5は、ルチル型のチタニア結晶相は確認されず、全てアナターゼ型結晶相であった。
試料1~17について、加熱振動試験を行った。加熱熱振動試験は、金属管の内面に無機多孔質層を形成した試料にて行った。具体的には、内径Φ55mm、外径Φ62mm(厚み3.5mm)、長さ80mmのパイプ(SUS430製、銅製)の外面をマスキングした状態で原料スラリーに浸漬し、無機多孔質層をパイプの内壁に塗布した。その後、200℃で乾燥、800℃で焼成して各試料を作製した。加熱振動試験は、試料を加熱振動試験装置に取り付け、加熱振動試験装置からプロパンの燃焼ガスをパイプ内に5分間流通させた後、常温エアガスを5分間流通させた。燃焼ガスは、パイプの流入側端面におけるガス温度が最大で900℃で、ガス流量が2.0Nm3/分となるように調整した。次に、上記燃焼ガスをパイプ内に連続して供給した状態で、長手方向(長さ方向)の振動をパイプに加えた。振動条件は100Hz、30Gとし、振動を50時間加えた。これらの条件で試験を行い、試験前後の重量変化率(重量減少率)を測定した。図4に、重量変化率が0.8%以下の試料に「〇」、重量変化率が0.8%超1%以下の試料に「△」、重量変化率が1%超の試料に「×」を付して示す。
試料1~17について、無機多孔質層と金属(金属板)の熱膨張係数を測定した。無機多孔質層の熱膨張係数測定用試料は、上記した原料スラリーを4mm×3mm×20mmのバルク体に成形した後、バルク体を800℃で焼成して作製した。金属の熱膨張係数測定用試料は、4mm×3mm×20mmのものを用いた。測定用試料は、熱膨張計を用いてJIS R1618(ファインセラミックスの熱機械分析による熱膨張の測定方法)に準拠して測定した。図5に、熱膨張係数の結果を示す。
試料1~17について、無機多孔質層と金属(金属板)の熱伝導率の測定を行った。熱伝導率も、無機多孔質層と金属板を別個のバルク体を用いて測定した。熱伝導率は、熱拡散率、比熱容量及び嵩密度を乗算し、算出した。熱拡散率は、レーザーフラッシュ法熱定数測定装置を用い、比熱容量はDSC(示差走査熱量計)を用いて、JIS R1611(ファインセラミックスのレーザーフラッシュ法による熱拡散率・比熱容量・熱伝導率試験方法)に準拠して室温で測定した。金属板の嵩密度は、φ10mm×厚み1mmのバルク体の重量を測定し、その重量を体積で割った値を嵩密度(単位:g/cm3)とした。また、無機多孔質層の嵩密度(単位:g/cm3)は下記式(3)から算出した。なお、熱拡散率は上記した原料スラリーをφ10mm×厚み1mmのバルク体に成形し、また、比熱容量は上記した原料スラリーをφ5mm×厚み1mmのバルク体に成形した後、それぞれのバルク体を800℃で焼成して熱拡散率および比熱容量測定用試料を作製し、測定した。測定結果を図5に示す。
式3:無機多孔質層の嵩密度=見掛け密度×(1-気孔率[%]/100)
式3:無機多孔質層の嵩密度=見掛け密度×(1-気孔率[%]/100)
図4に示すように、試料1~14,17は、焼成後の無機多孔質層にクラック及び剥離が確認されなかった。一方、試料15は、剥離は確認されなかったもののクラックの発生が確認された。また、試料16は、クラックと剥離の両方が確認された。この結果は、無機多孔質層内のアルミナ成分(セラミック繊維及び板状セラミック粒子)が少ない(15質量%未満)、又は、チタニア成分が少ない(45質量%未満)場合、焼成の際に金属-無機多孔質層間に力が作用し、無機多孔質層の特性が低下することを示している。具体的には、試料15は、アルミナ成分の割合が15質量%未満であるため、セラミック(粒子、繊維)間の結合力が低下し、無機多孔質層にクラックが発生したと推察される。また、試料16は、チタニア成分の割合が45質量%未満であるため、セラミック間の結合力が低下し、無機多孔質層にクラックが発生したと推察される。さらに試料16は、熱膨張係数が高いチタニア成分(チタニア粒子)の含有率が低く、金属に対する熱膨張係数比(α1/α2)が小さいので(0.5未満)、金属と無機多孔質層間の熱膨張差に基づいて無機多孔質層が金属から剥離したと推察される。以上より、セラミック繊維の種類(アルミナ繊維,ムライト繊維)及び板状セラミック粒子の種類(板状アルミナ粒子,板状マイカ)に係わらず、15質量%以上のアルミナ成分と45質量%以上のチタニア成分を含む無機多孔質層は、焼成後にクラック及び剥離等の劣化が生じにくくなることが確認された。
図4に示すように、試料1~4,7,8,10~14,17は、加熱振動試験後も無機多孔質層の劣化が確認されなかった。一方、試料5,6及び9は、焼成後の無機多孔質層にクラック及び剥離が確認されなかったが、加熱振動試験後の無機多孔質層の重量減少が大きくなることが確認された。一方、試料1~4,7,8,10~14,17は、焼成後の無機多孔質層にクラック及び剥離が確認されず、さらに、加熱振動試験後の無機多孔質層の重量減少も小さいことが確認された。試料5は、チタニア成分(アルミナ繊維,板状アルミナ粒子を結合させる結合材)にルチル型結晶相が含まれておらず(アナターゼ型結晶相であり)、高温のLPガスを流通させることによりチタニア結晶が相転移し、チタニア成分(結合材)の体積が変化したと推察される。また、試料6及び9は、他の試料1~4,7,8,10~14,17と比較して、合格レベルではあるが加熱振動試験後の無機多孔質層の重量減少が大きかった。試料6は、チタニア成分(アルミナ繊維,板状アルミナ粒子を結合させる結合材)を構成するルチル型結晶相が50質量%以下(40質量%)であり、アナターゼ型結晶相の割合が多い。そのため、高温のLPガスを流通させることによりチタニア結晶が相転移し、チタニア成分(結合材)の体積が変化したと推察される。その結果、無機多孔質層の一部が破損し、質量減少が生じたと推察される。なお、試料9は、ルチル型のチタニア結晶相が100質量%であるが、板状アルミナ粒子を含んでいないため、無機多孔質層が十分に補強されず、高温のLPガスを流通させた際に無機多孔質層の一部が破損したと推察される。以上より、無機多孔質層を構成するチタニア成分にルチル型結晶相が含まれていれば、振動及び熱衝撃に対する耐性が高い無機多孔質層が得られることが確認された。特に、ルチル型結晶相がチタニア成分の50質量%以上を占める無機多孔質層は、排気管に用いる無機多孔質層として最適であることが確認された。
以上、本発明の実施形態について詳細に説明したが、これらは例示に過ぎず、請求の範囲を限定するものではない。請求の範囲に記載の技術には、以上に例示した具体例を様々に変形、変更したものが含まれる。また、本明細書または図面に説明した技術要素は、単独であるいは各種の組合せによって技術的有用性を発揮するものであり、出願時請求項記載の組合せに限定されるものではない。また、本明細書または図面に例示した技術は複数目的を同時に達成するものであり、そのうちの一つの目的を達成すること自体で技術的有用性を持つものである。
2:金属管
4:無機多孔質層
10:排気管
4:無機多孔質層
10:排気管
Claims (9)
- 金属管と、金属管の内面の排気ガスが通過する部位に設けられている無機多孔質層と、を備えている排気管であって、
無機多孔質層は、
セラミック繊維を含み、
15質量%以上のアルミナ成分と45質量%以上のチタニア成分によって構成されており、
前記チタニア成分は、ルチル型結晶相を含んでいる排気管。 - ルチル型結晶相が、前記チタニア成分の50質量%以上を占めている請求項1に記載の排気管。
- 金属管の熱伝導率が、無機多孔質層の熱伝導率の100倍以上である請求項1または2に記載の排気管。
- 無機多孔質層の熱伝導率が、0.05W/mK以上3W/mK以下である請求項3に記載の排気管。
- 金属管の熱伝導率が、10W/mK以上400W/mK以下である請求項3または4に記載の排気管。
- 無機多孔質層の熱膨張係数をα1とし、金属管の熱膨張係数をα2としたときに、下記式(1)を満足する請求項1から5のいずれか一項に記載の排気管。
0.5<α1/α2<1.2 (1) - 無機多孔質層に、板状セラミック粒子が含まれている請求項1から6のいずれか一項に記載の排気管。
- 無機多孔質層に、0.1μm以上10μm以下の粒状粒子が含まれている請求項1から7のいずれか一項に記載の排気管。
- 無機多孔質層の表面に、被覆層が設けられている請求項1から8のいずれか一項に記載の排気管。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2022536402A JPWO2022014612A1 (ja) | 2020-07-13 | 2021-07-13 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2020120260 | 2020-07-13 | ||
| JP2020-120260 | 2020-07-13 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2022014612A1 true WO2022014612A1 (ja) | 2022-01-20 |
Family
ID=79555580
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2021/026359 Ceased WO2022014612A1 (ja) | 2020-07-13 | 2021-07-13 | 排気管 |
Country Status (2)
| Country | Link |
|---|---|
| JP (1) | JPWO2022014612A1 (ja) |
| WO (1) | WO2022014612A1 (ja) |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH06239656A (ja) * | 1993-02-12 | 1994-08-30 | Ibiden Co Ltd | 触媒用断熱材 |
| JP2002292242A (ja) * | 2001-04-02 | 2002-10-08 | Mitsubishi Chemicals Corp | 耐熱性マット及びその製造方法ならびに排気ガス浄化用触媒コンバータ |
| JP2018031346A (ja) * | 2016-08-26 | 2018-03-01 | トヨタ自動車株式会社 | 排気管 |
-
2021
- 2021-07-13 JP JP2022536402A patent/JPWO2022014612A1/ja active Pending
- 2021-07-13 WO PCT/JP2021/026359 patent/WO2022014612A1/ja not_active Ceased
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH06239656A (ja) * | 1993-02-12 | 1994-08-30 | Ibiden Co Ltd | 触媒用断熱材 |
| JP2002292242A (ja) * | 2001-04-02 | 2002-10-08 | Mitsubishi Chemicals Corp | 耐熱性マット及びその製造方法ならびに排気ガス浄化用触媒コンバータ |
| JP2018031346A (ja) * | 2016-08-26 | 2018-03-01 | トヨタ自動車株式会社 | 排気管 |
Also Published As
| Publication number | Publication date |
|---|---|
| JPWO2022014612A1 (ja) | 2022-01-20 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6813718B2 (ja) | 複合部材 | |
| US9028946B2 (en) | Ceramic honeycomb structure with applied inorganic skin | |
| JP5709391B2 (ja) | 多層熱的保護システム及び多層熱的保護システムを形成する方法 | |
| WO2022014613A1 (ja) | 排気管 | |
| US12153012B2 (en) | Gas sensor | |
| RU2754893C2 (ru) | Деталь, содержащая подложку и внешний барьер | |
| CN107428623A (zh) | 用于陶瓷衬底的热和环境障壁涂层 | |
| WO2005005019A1 (ja) | 排ガス浄化ハニカムフィルタ及びその製造方法 | |
| US20090011178A1 (en) | Honeycomb structure and bonding material to be used for same | |
| JP2006028002A (ja) | 耐食性窒化珪素セラミックス | |
| WO2007125667A1 (ja) | ハニカム構造体 | |
| US20220252540A1 (en) | Sensor element | |
| JP6423360B2 (ja) | 断熱膜、および断熱膜構造 | |
| WO2022014614A1 (ja) | 排気管 | |
| WO2022014611A1 (ja) | 複合部材 | |
| JP2022017128A (ja) | 複合部材 | |
| US20110143928A1 (en) | Catalytic filter or substrate containing silicon carbide and aluminum titanate | |
| WO2022014617A1 (ja) | 排気管 | |
| JP7743345B2 (ja) | 排気管 | |
| WO2022014615A1 (ja) | 排気管 | |
| WO2022014616A1 (ja) | 排気管 | |
| WO2015053242A1 (ja) | ガス流通部材 | |
| Vaubert et al. | Development of slurry-based Ca0. 5Sr0. 5Zr4 (PO4) 6 (CS-50) coatings for SiC in fossil energy applications | |
| JPH05253664A (ja) | セラミックス鋳ぐるみ部品 | |
| KR20150032801A (ko) | 열 노출 요소의 표면에 도포하기 위한 서멀 레지스트를 구비한 수단의 형성 방법 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 21841733 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2022536402 Country of ref document: JP Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 21841733 Country of ref document: EP Kind code of ref document: A1 |