EP2340332B1 - Vorrichtung zum imprägnieren von bahnförmigen materialien mit wärmehärtbarem imprägnierharz - Google Patents
Vorrichtung zum imprägnieren von bahnförmigen materialien mit wärmehärtbarem imprägnierharz Download PDFInfo
- Publication number
- EP2340332B1 EP2340332B1 EP09783817A EP09783817A EP2340332B1 EP 2340332 B1 EP2340332 B1 EP 2340332B1 EP 09783817 A EP09783817 A EP 09783817A EP 09783817 A EP09783817 A EP 09783817A EP 2340332 B1 EP2340332 B1 EP 2340332B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- impregnating
- trough
- resin
- web
- heating device
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 229920005989 resin Polymers 0.000 title claims abstract description 63
- 239000011347 resin Substances 0.000 title claims abstract description 63
- 239000000463 material Substances 0.000 title claims abstract description 44
- 238000010438 heat treatment Methods 0.000 claims abstract description 23
- 238000005470 impregnation Methods 0.000 claims description 24
- 238000001816 cooling Methods 0.000 claims description 21
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 6
- 230000005855 radiation Effects 0.000 claims description 3
- 238000005507 spraying Methods 0.000 claims description 3
- 238000004519 manufacturing process Methods 0.000 description 11
- 238000001035 drying Methods 0.000 description 7
- 239000002904 solvent Substances 0.000 description 6
- 238000011161 development Methods 0.000 description 5
- 230000035515 penetration Effects 0.000 description 5
- 239000007787 solid Substances 0.000 description 5
- 230000015572 biosynthetic process Effects 0.000 description 4
- 238000000034 method Methods 0.000 description 4
- 229920001568 phenolic resin Polymers 0.000 description 4
- 230000007704 transition Effects 0.000 description 4
- 238000011144 upstream manufacturing Methods 0.000 description 4
- 239000007795 chemical reaction product Substances 0.000 description 3
- 238000000576 coating method Methods 0.000 description 3
- KXGFMDJXCMQABM-UHFFFAOYSA-N 2-methoxy-6-methylphenol Chemical compound [CH]OC1=CC=CC([CH])=C1O KXGFMDJXCMQABM-UHFFFAOYSA-N 0.000 description 2
- 229920000877 Melamine resin Polymers 0.000 description 2
- 229920001807 Urea-formaldehyde Polymers 0.000 description 2
- 239000002131 composite material Substances 0.000 description 2
- 238000001514 detection method Methods 0.000 description 2
- 229920003002 synthetic resin Polymers 0.000 description 2
- 239000000057 synthetic resin Substances 0.000 description 2
- 229920001187 thermosetting polymer Polymers 0.000 description 2
- DGXAGETVRDOQFP-UHFFFAOYSA-N 2,6-dihydroxybenzaldehyde Chemical compound OC1=CC=CC(O)=C1C=O DGXAGETVRDOQFP-UHFFFAOYSA-N 0.000 description 1
- 239000004640 Melamine resin Substances 0.000 description 1
- 239000000654 additive Substances 0.000 description 1
- GZCGUPFRVQAUEE-SLPGGIOYSA-N aldehydo-D-glucose Chemical compound OC[C@@H](O)[C@@H](O)[C@H](O)[C@@H](O)C=O GZCGUPFRVQAUEE-SLPGGIOYSA-N 0.000 description 1
- 229920003180 amino resin Polymers 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000004744 fabric Substances 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- HANVTCGOAROXMV-UHFFFAOYSA-N formaldehyde;1,3,5-triazine-2,4,6-triamine;urea Chemical compound O=C.NC(N)=O.NC1=NC(N)=NC(N)=N1 HANVTCGOAROXMV-UHFFFAOYSA-N 0.000 description 1
- HMJMQKOTEHYCRN-UHFFFAOYSA-N formaldehyde;phenol;1,3,5-triazine-2,4,6-triamine;urea Chemical compound O=C.NC(N)=O.OC1=CC=CC=C1.NC1=NC(N)=NC(N)=N1 HMJMQKOTEHYCRN-UHFFFAOYSA-N 0.000 description 1
- 238000007654 immersion Methods 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 239000004848 polyfunctional curative Substances 0.000 description 1
- 238000006116 polymerization reaction Methods 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 239000000047 product Substances 0.000 description 1
- 238000009420 retrofitting Methods 0.000 description 1
- 238000000518 rheometry Methods 0.000 description 1
- 229920002050 silicone resin Polymers 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 239000012209 synthetic fiber Substances 0.000 description 1
- 229920002994 synthetic fiber Polymers 0.000 description 1
- 235000018553 tannin Nutrition 0.000 description 1
- 229920001864 tannin Polymers 0.000 description 1
- 239000001648 tannin Substances 0.000 description 1
- 238000012546 transfer Methods 0.000 description 1
- 239000002023 wood Substances 0.000 description 1
Images
Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H17/00—Non-fibrous material added to the pulp, characterised by its constitution; Paper-impregnating material characterised by its constitution
- D21H17/20—Macromolecular organic compounds
-
- D—TEXTILES; PAPER
- D06—TREATMENT OF TEXTILES OR THE LIKE; LAUNDERING; FLEXIBLE MATERIALS NOT OTHERWISE PROVIDED FOR
- D06B—TREATING TEXTILE MATERIALS USING LIQUIDS, GASES OR VAPOURS
- D06B3/00—Passing of textile materials through liquids, gases or vapours to effect treatment, e.g. washing, dyeing, bleaching, sizing, impregnating
- D06B3/10—Passing of textile materials through liquids, gases or vapours to effect treatment, e.g. washing, dyeing, bleaching, sizing, impregnating of fabrics
-
- D—TEXTILES; PAPER
- D06—TREATMENT OF TEXTILES OR THE LIKE; LAUNDERING; FLEXIBLE MATERIALS NOT OTHERWISE PROVIDED FOR
- D06C—FINISHING, DRESSING, TENTERING OR STRETCHING TEXTILE FABRICS
- D06C7/00—Heating or cooling textile fabrics
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H19/00—Coated paper; Coating material
- D21H19/10—Coatings without pigments
- D21H19/14—Coatings without pigments applied in a form other than the aqueous solution defined in group D21H19/12
- D21H19/24—Coatings without pigments applied in a form other than the aqueous solution defined in group D21H19/12 comprising macromolecular compounds obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H21/00—Non-fibrous material added to the pulp, characterised by its function, form or properties; Paper-impregnating or coating material, characterised by its function, form or properties
- D21H21/14—Non-fibrous material added to the pulp, characterised by its function, form or properties; Paper-impregnating or coating material, characterised by its function, form or properties characterised by function or properties in or on the paper
- D21H21/16—Sizing or water-repelling agents
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H23/00—Processes or apparatus for adding material to the pulp or to the paper
- D21H23/02—Processes or apparatus for adding material to the pulp or to the paper characterised by the manner in which substances are added
- D21H23/22—Addition to the formed paper
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H25/00—After-treatment of paper not provided for in groups D21H17/00 - D21H23/00
- D21H25/02—Chemical or biochemical treatment
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H27/00—Special paper not otherwise provided for, e.g. made by multi-step processes
- D21H27/18—Paper- or board-based structures for surface covering
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C—APPARATUS FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C3/00—Apparatus in which the work is brought into contact with a bulk quantity of liquid or other fluent material
- B05C3/02—Apparatus in which the work is brought into contact with a bulk quantity of liquid or other fluent material the work being immersed in the liquid or other fluent material
- B05C3/12—Apparatus in which the work is brought into contact with a bulk quantity of liquid or other fluent material the work being immersed in the liquid or other fluent material for treating work of indefinite length
- B05C3/125—Apparatus in which the work is brought into contact with a bulk quantity of liquid or other fluent material the work being immersed in the liquid or other fluent material for treating work of indefinite length the work being a web, band, strip or the like
Definitions
- the invention relates to a device for impregnating web-like material with thermosetting impregnating resin comprising a impregnating trough in which the web-like material is brought into contact with the impregnating resin, a supply line leading to the impregnating trough, through which the impregnating resin is introduced into the impregnating trough, a heating device which heats the impregnating resin.
- impregnation of web-like material with heat-curable impregnating resin serves to produce impregnates, such as are used individually or in the form of a laminate formed from such impregnates, for example for coating base bodies formed from wood-based material, for example during manufacture of panels for covering surfaces, for example floors.
- the web material is not only in the prior art, but also in connection with the present invention, in particular a composite of natural fibers and / or synthetic fibers composite into consideration, for example, a scrim, a mat, a fabric or the like.
- the web material is paper whose basis weight in the unimpregnated state can be between about 25 g / m 2 and about 300 g / m 2 .
- the paper layer of an impregnate which is intended to form a visible surface of the end product, can be printed with a desired décor.
- the impregnating resin is mixed with a solvent, for example water, whose function is to lower the viscosity of the synthetic resin.
- a solvent for example water
- the impregnating liquor thus formed may, if desired, be admixed with further additives, for example a hardener.
- the finished impregnated web material must be dried before further processing, i. the solvent must be removed from the impregnate again so that only the impregnating resin of the impregnating liquor remains in the finished product.
- the web material is impregnated with impregnating resin or that impregnating resin penetrates into the web material
- the web material is impregnated with impregnating filament or that the impregnating liquor penetrates into the web material.
- the impregnating resin has also penetrated the web material and remains there during subsequent drying.
- the solvent which is based on a given amount of resin and has to be additionally added to reduce the viscosity, must again be removed from the impregnated web-like material in the subsequent drying step. This costs energy and time and thus in turn contributes to an increase in the cost of the impregnate. Overall, therefore, there is no cost advantage.
- the increase in temperature are also limited in practice. Namely, the impregnating resin cures faster at higher temperature, i. it polymerizes faster. However, the higher the molecular weight of the resin, the worse it penetrates into the web-like material and the worse the finished impregnate can be further processed later. Thus, for example, at a temperature of the impregnating trough of more than 35 ° C, the liquor life is reduced to such an extent that in the event of a stoppage of production, the impregnating liquor would become unusable so quickly that disposal of the whole in the production plant, i. especially in the impregnating trough, existing impregnating liquor would be required. Of course, this is not tolerable.
- thermosetting impregnating resin it is therefore an object of the present invention to develop a device of the generic type such that the impregnation of sheet material with thermosetting impregnating resin can be made more effective.
- the heating device is associated with the feed line and heated the impregnating resin in the feed line.
- the impregnating resin is no longer heated in the impregnating trough, but in a heating device upstream of the impregnating trough.
- the wall surfaces of the impregnating trough no longer need to be used as heat exchanger surfaces for heating the impregnating resin, so that the risk of formation of coatings on these walls is at least reduced, if not completely excluded.
- the impregnating resin more precisely the impregnating liquor
- the impregnating trough having a higher temperature, in particular a temperature of between approximately 50 ° C. and approximately 80 ° C., and thus lower viscosity than was possible in the prior art.
- the penetration of the impregnating resin into the web-shaped material can be improved.
- the impregnating liquor may also contain less solvent and, due to the elevated temperature, have a viscosity which corresponds to that of a prior art impregnating liquor with a higher solvent content and lower temperature. This allows the subsequent drying to run more effectively.
- these two effects can also be used together.
- the impregnation process is carried out Use of the impregnating device according to the invention run off more effectively.
- the impregnation process itself is faster, thereby increasing the amount of sheet-like material impregnated per unit time.
- the drying of the impregnated web-shaped material can be done faster and with the use of less energy.
- the heating device is a non-contact heating device.
- the heating device can heat the impregnating resin, for example using microwave radiation.
- a control device which ensures that the heating device is supplied only to the amount of impregnating resin required for impregnation.
- the control device may operate in response to the detection signal of at least one sensor detecting at least one operating parameter of the impregnation device, for example, depending on the engine speed, i. depending on the speed with which the sheet material is fed to the impregnating trough.
- the control device can also be connected to a pump, which supplies the heating device with the amount of impregnating resin required for impregnation, or further functional units of the impregnating device.
- the impregnating trough be provided with a cooling device.
- This cooling device can be used, for example in the case of a production stoppage, to cool the impregnating resin in order to reduce its polymerization rate and thereby increase the liquor service life in such a way that that the resin can still be used after the resumption of production.
- This cooling device may comprise an integrated cooling unit.
- the heat exchanger device already present in impregnating tanks of the prior art can no longer be used for heating but rather for cooling the impregnating liquor.
- the cooling device comprises an external cooling unit. This can be particularly advantageous if particularly high cooling capacities are required.
- the impregnating liquor or the impregnating resin is pumped out of the impregnating trough and through the external cooling unit in order to be able to achieve an even more effective cooling.
- the impregnation tank is subdivided into at least two sub-tanks. This makes it possible to use a first part-tub for pre-impregnation and a second part-tub for main impregnation, wherein the impregnating resin can be kept preferably only in the first part-tub at the elevated temperature compared to the prior art, while in the second part-tub at a temperature which corresponds, for example, to the temperature used in the prior art.
- a first sub-trough connected to the feed line to have a smaller volume than a further sub-trough arranged further downstream in the flow direction of the resin.
- a further cooling unit is arranged between the two sub-wells.
- the further cooling unit can be assigned to a third part trough serving as a transition part trough, wherein this transition part trough, for example, can still be attributed to the preimpregnation step.
- the receiving volumes of the plurality of sub-pans can be formed separately from each other, in such a way that on the one hand a transition of impregnating from an upstream sub-tub to a downstream sub-tub can be done, but on the other hand, a transition of impregnating from a downstream sub-tub to one upstream arranged sub-tub is not possible.
- a spraying device which moistens the sheet-like material, for example with water, preferably hot water or steam.
- the use of the impregnating device according to the invention enables the impregnation at a significantly higher solids content of the impregnating liquor, which can be saved in the subsequent drying considerable amounts of energy or allow existing drying capacities higher production speeds. For example, it is possible to work with a solids content of about 60% of impregnating resin in the impregnating liquor.
- aminoplast and phenoplast resins are usually used as impregnating resins.
- the following resins may be considered as impregnating resins: urea-formaldehyde resin, melamine-formaldehyde resin, melamine-urea-formaldehyde resin (MUF), melamine-urea-phenol-formaldehyde resin (MUPF), phenol-formaldehyde Resin (PF), tannin resins, resorcinol-formaldehyde resins, silicone resins.
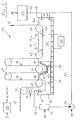
- Fig. 1 is a device for impregnating a sheet material 12, for example a paper web, generally designated 10.
- the impregnating device 10 comprises an impregnating trough 14, in which the paper web 12 is impregnated with impregnating resin 16, more precisely, impregnating liquor 16a.
- the impregnating trough 14 is subdivided in the illustrated embodiment into three sub-troughs 18, 20 and 22, which are passed through in succession from the material web 12 along a predetermined path of deflection rollers 24.
- the guide rollers 24 correspond to those of an impregnating device of the prior art. Therefore, a more detailed explanation in this regard will be omitted here.
- the impregnation device 10 includes a tub body 26 having a well volume 26a.
- an insert body 28 is inserted, in which the first part trough 18 and the second part trough 20 are formed.
- the partial volume of the tub volume 26a not occupied by the insert body 28 forms the third part tub 22.
- the volume of the first part tub 18 is smaller than the volume of the second part tub 20, and the latter is again smaller than the volume of the third part tub 22.
- the first part trough 18 is supplied via an inlet line 30 to the impregnating liquor 16a, which has previously been heated without contact in a heating device 32, preferably by means of microwave radiation.
- the inlet of the feed line 30 into the first part of the trough 18 is shown at 34.
- the impregnating liquor 16a may comprise about 60% solids content of impregnating resin 16, for example melamine resin, in a solvent, for example water, and be introduced into the first part trough 18 at a temperature of about 50 ° C. to 80 ° C.
- the impregnating liquor 16a Due to this high temperature, the impregnating liquor 16a, despite the high solids content, has such a low viscosity that it can easily penetrate into the material web 12 in the first sub-tub 18 in order to impregnate it.
- the material web 12 may be moistened before entry into the first part trough 18 by means of a spray device 36 and, if desired, also preheated.
- the impregnating liquor passes from the first part-trough 18 into the second part-trough 20 via an overflow 38.
- the boundary walls 20a of the second part-wall 20 are designed as heat-exchanging surfaces of a cooling unit 40, which cools the impregnating liquor 16a to a temperature of about 30 ° C., for its service life to increase significantly.
- a cooling unit 40 which cools the impregnating liquor 16a to a temperature of about 30 ° C., for its service life to increase significantly.
- the web 12 in the second sub-tub 20 soaked again with impregnating liquor 16 a.
- the impregnating liquor 16a passes from the second sub-tub 20 into the third sub-tub 22, in which a dip section 44 is provided for the material web 12. While the actual impregnation of the material web 12 takes place with impregnating liquor 16a in the first two sub-troughs 18 and 20, the main function of the immersion path 44 in the third sub-trough 22 is to ensure that the material web 12 is loaded with the desired amount of impregnating liquor 16a.
- doctor blades 46 are provided, the task of which is to remove excess impregnating liquor 16a from the surface of the material web 12 and / or evenly distribute and / or smooth the impregnating liquor 16a applied to the material web 12, the present invention is not concerned with this aspect. Therefore, a more detailed explanation will be omitted in this regard.
- a cooling device 48 is provided in the bottom of the impregnating trough 26, the task of which is to keep the impregnating liquor 16a in the third partial volume 22 at the desired temperature of about 30 ° C, which in the case of a production standstill on the other hand but also is used to cool the impregnating liquor 16a even further, in order to increase their service life so far that they can be used loss-free after resumption of production.
- an external cooling device 50 can also be provided for this purpose, which pumps and cools the impregnating liquor 16a from the trough volume 26a.
- the impregnating liquor 16a is pumped around. In fact, it is removed via a drain 52 from the tub volume 26a and via a line 54 from a pump 56 to the microwave heating device 32 and passed via the supply line 30 on to the inlet 34 into the first part trough 18.
- the pump 56 and the microwave heating device 32 preferably operate under the control of a control unit 58, so that on the one hand it is ensured that always exactly the amount of impregnating liquor 16a is introduced into the first part pan 18, depending on the production speed, in particular the running speed the material web 12 is required, and that the impregnating liquor 16a is introduced into the first part trough 18 at the desired temperature.
- a metering device 60 ensures that via a line 62 and an inlet 64 always exactly the amount of impregnating liquor 16 is replenished into the tub volume 26a, which removes the material web 12 as a result of impregnation from the impregnating device 10. In this way it can be ensured that the mirror of the impregnation liquor 16 in the sub-tanks 18, 20 and 22 can always be kept at the same height.
- the metering device 60 also preferably operates under the control of the control device 58.
- the detection signals of a plurality of sensors S are supplied, for example, a sensor for detecting the speed of the web 12, a sensor for detecting the temperature of the introduced into the first sub-tub 18 impregnating liquor 16a, a sensor for detecting the level of the impregnating liquor 16a in the sub-wells 18, 20 and 22 and the like sensors more.
- sensors and their connection lines to the control device 58 are in Fig. 1 not shown for reasons of clarity of presentation.
- FIG. 1 illustrated embodiment for retrofitting to existing impregnation devices of the prior art.
- the insert body 28 in which the first two sub-wells 18 and 20 are formed needs in the Tray volume 26a of the impregnating trough 26 to be used to make a impregnating device of the prior art, an impregnating device 10 according to the invention.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Life Sciences & Earth Sciences (AREA)
- Biochemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Paper (AREA)
- Reinforced Plastic Materials (AREA)
- Treatment Of Fiber Materials (AREA)
Abstract
Description
- Die Erfindung betrifft eine Vorrichtung zum Imprägnieren bahnförmigen Materials mit wärmehärtbarem Imprägnierharz, umfassend eine Imprägnierwanne, in welcher das bahnförmige Material mit dem Imprägnierharz in Kontakt gebracht wird, eine zur Imprägnierwanne führende Zulaufleitung, durch welche das Imprägnierharz in die Imprägnierwanne eingeleitet wird, eine Erwärmungsvorrichtung, welche das Imprägnierharz erwärmt.
- Derartige Vorrichtungen sind aus der Praxis allgemein bekannt.
- Das Imprägnieren bahnförmigen Materials mit wärmehärtbarem Imprägnierharz dient zusammen mit der anschließenden Trocknung des imprägnierten bahnförmigen Materials der Herstellung von Imprägnaten, wie sie einzeln oder in Form eines aus solchen Imprägnaten gebildeten Laminats beispielsweise zur Beschichtung von aus Holzwerkstoff gebildeten Grundkörpern verwendet werden, so etwa bei der Herstellung von Paneelen zur Verkleidung von Oberflächen, beispielsweise Fußböden.
- Als Bahnmaterial kommt dabei nicht nur beim Stand der Technik, sondern auch im Zusammenhang mit der vorliegenden Erfindung insbesondere ein aus Naturfasern oder/und Kunstfasern gebildeter Verbund in Betracht, beispielsweise ein Gelege, eine Matte, ein Gewebe oder dergleichen. Vorzugsweise handelt es sich bei dem Bahnmaterial um Papier, dessen Flächengewicht im nicht imprägnierten Zustand zwischen etwa 25 g/m2 und etwa 300 g/m2 betragen kann. Bekanntermaßen kann die Papierlage eines Imprägnats, das zur Bildung einer Sichtfläche des Endprodukts bestimmt ist, mit einem gewünschten Dekor bedruckt sein.
- Um das Eindringen des Imprägnierharzes in das Bahnmaterial ermöglichen zu können, ist das Imprägnierharz mit einem Lösungsmittel, beispielsweise Wasser, versetzt, dessen Funktion es ist, die Viskosität des Kunstharzes zu senken. Der so gebildeten Imprägnierflotte können gewünschtenfalls noch weitere Zusatzstoffe beigemengt werden, beispielsweise ein Härter. Das fertig imprägnierte Bahnmaterial muss vor der Weiterverarbeitung getrocknet werden, d.h. das Lösungsmittel muss wieder aus dem Imprägnat entfernt werden, so dass von der Imprägnierflotte nur noch das Imprägnierharz im fertigen Produkt verbleibt.
- Wenn im Zusammenhang mit der vorliegenden Erfindung nachstehend davon die Rede ist, dass das Bahnmaterial mit Imprägnierharz getränkt wird oder dass Imprägnierharz in das Bahnmaterial eindringt, so ist damit gemeint, dass das Bahnmaterial mit Imprägnierfilotte getränkt wird bzw. dass die Imprägnierflotte in das Bahnmaterial eindringt. Im Hinblick auf das Endprodukt kommt es aber letzten Endes nur darauf an, dass dabei auch das Imprägnierharz das Bahnmaterial durchdrungen hat und beim anschließenden Trocknen in diesem verbleibt. Ferner sei an dieser Stelle darauf hingewiesen, dass obgleich im Zusammenhang mit der vorliegenden Erfindung immer von "dem Kunstharz" bzw. "dem Imprägnierharz" in der Einzahl gesprochen wird, dieses Harz auch eine Mischung verschiedener Kunstharze sein kann.
- Wie bei jedem anderen industriell genutzten Prozess muss auch bei der Herstellung von Imprägnaten versucht werden, diesen Prozess möglichst schnell und effektiv ablaufen zu lassen, um den hierdurch verursachten Kostenanteil am Endprodukt möglichst niedrig halten zu können. Hierzu ist es von zentraler Bedeutung, das bahnförmige Material möglichst schnell und effektiv mit dem Imprägnierharz tränken und anschließend trocknen zu können. Die zum Imprägnieren benötigte Zeit ist bekanntermaßen um so niedriger, je geringer die Viskosität der Imprägnierflotte ist. Zur Erzielung einer möglichst niedrigen Viskosität der Imprägnierflotte kann zum einen deren Feststoffanteil, d.h. Harzanteil gesenkt und zum anderen deren Temperatur erhöht werden.
- Das bezogen auf eine vorgegebene Harzmenge bezogene, zur Verringerung der Viskosität zusätzlich zuzusetzende Lösungsmittel muss in dem nachfolgenden Trocknungsschritt wieder aus dem imprägnierten bahnförmigen Material entfernt werden. Dies kostet Energie und Zeit und trägt somit wiederum zu einer Erhöhung der Kosten für das Imprägnat bei. Insgesamt ergibt sich daher kein Kostenvorteil.
- Aber auch der Erhöhung der Temperatur sind in der Praxis Grenzen gesetzt. Das Imprägnierharz härtet nämlich bei höherer Temperatur schneller, d.h. es polymerisiert schneller aus. Je höher aber das Molekulargewicht des Harzes ist, desto schlechter dringt es in das bahnförmige Material ein und desto schlechter lässt sich das fertige Imprägnat später weiterverarbeiten. So ist beispielsweise bei einer Temperatur der Imprägnierwanne von mehr als 35°C die Flottenstandzeit so weit reduziert, dass im Falle einer Produktionsunterbrechung die Imprägnierflotte so rasch unbrauchbar würde, dass eine Entsorgung der gesamten in der Produktionsanlage, d.h. insbesondere in der Imprägnierwanne, vorhandenen Imprägnierflotte erforderlich wäre. Dies ist selbstverständlich nicht tolerierbar.
- Ein weiteres Problem, das im Stand der Technik bereits bei den derzeit üblichen Wannentemperaturen von höchstens 35°C auftritt, besteht darin, dass durch die hohen Harzdurchsätze von bis zu 2000 kg Flotte/h die Wärmetauscherflächen der Imprägnierwanne recht heiß sein müssen, um die in der Imprägnierwanne aufgenommene Imprägnierflotte auf die gewünschte Wannentemperatur bringen zu können. Da durch die geometrische Gestaltung der Wannen naturgemäß laminare Strömungsbereiche und in ungünstigen Fällen sogar Toträume existieren, kommt es an den Wärmetauscherflächen immer wieder zur Bildung von Harzbelägen, welche den Wärmeübergang im Laufe der Zeit immer weiter verschlechtern. Dadurch beginnt ein Teufelskreis aus immer höher werdenden notwendigen Temperaturen an den Wärmetauscherflächen und dadurch immer rascher stattfindender Belagsbildung - die Wanne "wächst zu".
- Es ist daher Aufgabe der vorliegenden Erfindung, eine Vorrichtung der gattungsgemäßen Art derart weiterzubilden, dass das Imprägnieren von bahnförmigem Material mit wärmehärtbarem Imprägnierharz effektiver vorgenommen werden kann.
- Diese Aufgabe wird erfindungsgemäß durch eine Vorrichtung der eingangs genannten Art gelöst, bei welcher die Erwärmungsvorrichtung der Zulaufleitung zugeordnet ist und das Imprägnierharz in der Zulaufleitung erwärmt. Erfindungsgemäß wird also das Imprägnierharz nicht mehr in der Imprägnierwanne erwärmt, sondern in einer der Imprägnierwanne vorgeordneten Erwärmungsvorrichtung. Hierdurch brauchen die Wandungsflächen der Imprägnierwanne nicht mehr als Wärmetauscherflächen zur Erwärmung des Imprägnierharzes genutzt zu werden, so dass die Gefahr einer Bildung von Belägen an diesen Wandungen zumindest reduzierbar, wenn nicht gar vollständig ausgeschlossen ist.
- Somit ist es möglich, das Imprägnierharz, genauer gesagt die Imprägnierflotte, der Imprägnierwanne mit einer höheren Temperatur, insbesondere einer Temperatur von zwischen etwa 50°C und etwa 80°C, und somit niedrigeren Viskosität zuzuführen als dies beim Stand der Technik möglich war. Hierdurch kann das Eindringverhalten des Imprägnierharzes in das bahnförmige Material verbessert werden. Alternativ kann die Imprägnierflotte aber auch weniger Lösungsmittel enthalten und aufgrund der erhöhten Temperatur eine Viskosität aufweisen, welche jener einer Imprägnierflotte des Standes der Technik mit höherem Lösungsmittelanteil und niedrigerer Temperatur entspricht. Hierdurch kann die anschließende Trocknung effektiver ablaufen. Selbstverständlich können diese beiden Effekte auch miteinander kombiniert angewendet werden. In welcher Form auch immer man die vorteilhaften Folgen der durch die vorliegende Erfindung ermöglichten Temperaturerhöhung ausnutzt, in jedem Fall wird der Imprägnierprozess durch Einsatz der erfindungsgemäßen Imprägniervorrichtung effektiver ablaufen. Im erstgenannten Fall läuft der Imprägnierprozess selbst schneller ab, wodurch die Menge an pro Zeiteinheit imprägniertem bahnförmigem Material erhöht wird. Und im anderen Fall kann die Trocknung des imprägnierten bahnförmigen Materials schneller und unter Einsatz von weniger Energie vorgenommen werden.
- Um auch in der der Imprägnierwanne vorgeschalteten Erwärmungsvorrichtung die Bildung von Belägen verhindern zu können, wird in Weiterbildung der Erfindung vorgeschlagen, dass die Erwärmungsvorrichtung eine berührungslos arbeitende Erwärmungsvorrichtung ist. Hierzu kann die Erwärmungsvorrichtung das Imprägnierharz beispielsweise unter Einsatz von Mikrowellenstrahlung erwärmen.
- Ferner kann es vorteilhaft sein, wenn eine Steuervorrichtung vorgesehen ist, welche dafür sorgt, dass der Erwärmungseinrichtung nur die zum Imprägnieren benötigte Menge an Imprägnierharz zugeführt wird. Hierdurch kann insbesondere die für die Erwärmung des Imprägnierharzes aufgewendete Energiemenge auf ein Minimum reduziert werden. Die Steuervorrichtung kann in Abhängigkeit von dem Erfassungssignal wenigstens eines Sensors arbeiten, der wenigstens einen Betriebsparameter der Imprägniervorrichtung erfasst, beispielsweise in Abhängigkeit von der Maschinengeschwindigkeit, d.h. in Abhängigkeit von der Geschwindigkeit, mit der das bahnförmige Material der Imprägnierwanne zugeführt wird. Die Steuervorrichtung kann ferner mit einer Pumpe verbunden sein, die der Erwärmungseinrichtung die zum Imprägnieren benötigte Menge an Imprägnierharz zuführt, oder weiteren Funktionseinheiten der Imprägniervorrichtung.
- In Weiterbildung der Erfindung wird vorgeschlagen, dass die Imprägnierwanne mit einer Kühlvorrichtung versehen ist. Diese Kühlvorrichtung kann beispielsweise im Falle einer Produktionsunterbrechung dazu genutzt werden, das Imprägnierharz abzukühlen, um seine Polymerisationsgeschwindigkeit zu reduzieren und dadurch die Flottenstandzeit derart zu erhöhen, dass das Harz auch nach der Wiederaufnahme der Produktion noch weiter verwendet werden kann.
- Diese Kühlvorrichtung kann eine integrierte Kühleinheit umfassen. So kann beispielsweise die bei Imprägnierwannen des Standes der Technik bereits vorhandene Wärmetauschervorrichtung nun erfindungsgemäß nicht mehr zum Erwärmen, sondern vielmehr zum Kühlen der Imprägnierflotte genutzt werden.
- Zusätzlich oder alternativ ist es jedoch auch möglich, dass die Kühlvorrichtung eine externe Kühleinheit umfasst. Dies kann insbesondere dann von Vorteil sein, wenn besonders hohe Kühlleistungen erforderlich sind. Die Imprägnierflotte bzw. das Imprägnierharz wird in diesem Fall aus der Imprägnierwanne heraus und durch die externe Kühleinheit gepumpt, um eine noch effektivere Kühlung erzielen zu können.
- In Weiterbildung der Erfindung wird ferner vorgeschlagen, dass die Imprägnierwanne in wenigstens zwei Teilwannen unterteilt ist. Dies ermöglicht es, eine erste Teilwanne zum Vorimprägnieren und eine zweite Teilwanne zum Hauptimprägnieren zu nutzen, wobei das Imprägnierharz bevorzugt lediglich in der ersten Teilwanne auf der im Vergleich zum Stand der Technik erhöhten Temperatur gehalten werden kann, während es in der zweiten Teilwanne auf einer Temperatur gehalten wird, die beispielsweise der im Stand der Technik verwendeten Temperatur entspricht. Diese Weiterbildung macht sich zunutze, dass das eigentliche Eindringen der Imprägnierflotte in das bahnförmige Material bereits im Vorimprägnierschritt erfolgt und es im Hauptimprägnierschritt hauptsächlich noch um die richtige Dosierung des Flächengewichts des Imprägnierharzes relativ zum Flächengewicht des bahnförmigen Materials geht.
- Daher ist es auch möglich, dass eine mit der Zulaufleitung verbundene erste Teilwanne ein kleineres Volumen aufweist als eine in Strömungsrichtung des Harzes weiter stromabwärts angeordnete weitere Teilwanne. Vorteilhaft ist es ferner, wenn zwischen den beiden Teilwannen eine weitere Kühleinheit angeordnet ist. Gewünschtenfalls kann die weitere Kühleinheit einer dritten, als Übergangsteilwanne dienenden Teilwanne zugeordnet sein, wobei diese Übergangsteilwanne beispielsweise noch dem Vorimprägnierschritt zugerechnet werden kann.
- Vorteilhafterweise können die Aufnahmevolumina der Mehrzahl von Teilwannen voneinander getrennt ausgebildet sein, und zwar derart, dass zwar einerseits ein Übergang von Imprägnierflotte von einer stromaufwärts angeordneten Teilwanne zu einer stromabwärts angeordneten Teilwanne erfolgen kann, andererseits aber ein Übergang von Imprägnierflotte von einer stromabwärts angeordneten Teilwanne zu einer stromaufwärts angeordneten Teilwanne nicht möglich ist.
- In Weiterbildung der Erfindung kann schließlich auch noch eine Sprühvorrichtung vorgesehen sein, welche das bahnförmige Material befeuchtet, beispielsweise mit Wasser, vorzugsweise heißem Wasser oder Wasserdampf. Durch diese Maßnahme kann das Eindringen der Imprägnierflotte in das bahnförmige Material weiter verbessert werden. Besonders vorteilhaft ist es in diesem Fall, wenn das bahnförmige Material sowohl vorbefeuchtet als auch vorgewärmt wird.
- Der Einsatz der erfindungsgemäßen Imprägniervorrichtung ermöglicht die Imprägnierung bei deutlich höherem Feststoffgehalt der Imprägnierflotte, wodurch bei der anschließenden Trocknung erhebliche Energiemengen eingespart werden können bzw. bereits bestehende Trocknungskapazitäten höhere Produktionsgeschwindigkeiten erlauben. Beispielsweise kann mit einem Feststoffgehalt von etwa 60% Imprägnierharz in der Imprägnierflotte gearbeitet werden.
- Darüber hinaus wurde überraschend festgestellt, dass sich die Rheologie der Imprägnierflotte bei höheren Temperaturen vorteilhaft verändert. So kam es bei herkömmlichen Imprägniervorrichtungen durch das Herumspritzen des Harzes im Imprägnierbereich ständig zu Verschmutzungen und Beschädigungen. Erfindungsgemäß wurde nun überraschend festgestellt, dass bei höheren Temperaturen die Spritzneigung der Imprägnierflotte abnimmt und dadurch deutlich längere Wartungsintervalle der Imprägniervorrichtung möglich werden.
- Nachzutragen ist noch, dass als Imprägnierharze üblicherweise Aminoplast- und Phenoplastharze eingesetzt werden. Beispielsweise können folgende Harze als Imprägnierharze in Betracht kommen: Harnstoff-Formaldehyd-Harz, Melamin-Formaldehyd-Harz, Melamin-Harnstoff-Formaldehyd-Harz (MUF), Melamin-Harnstoff-Phenol-Formaldehyd-Harz (MUPF), Phenol-Formaldehyd-Harz (PF), Tanninharze, Resorcinol-Formaldehyd-Harze, Silikonharze.
- Die Erfindung wird im Folgenden an einem Ausführungsbeispiel mit Bezug auf die beigefügte Zeichnung näher erläutert werden. Es stellt dar:
- Fig. 1
- eine schematische Darstellung des Aufbaus einer erfindungsgemäßen Imprägniervorrichtung.
- In
Fig. 1 ist eine Vorrichtung zum Imprägnieren eines bahnförmigen Materials 12, beispielsweise einer Papierbahn, ganz allgemein mit 10 bezeichnet. Die Imprägniervorrichtung 10 umfasst eine Imprägnierwanne 14, in welcher die Papierbahn 12 mit Imprägnierharz 16, genauer gesagt Imprägnierflotte 16a, getränkt wird. - Die Imprägnierwanne 14 ist in dem dargestellten Ausführungsbeispiel in drei Teilwannen 18, 20 und 22 unterteilt, welche von der Materialbahn 12 längs eines von Umlenkwalzen 24 vorgegebenen Bahnverlaufs nacheinander durchlaufen werden. Hinsichtlich ihres Aufbaus und ihrer Anordnung und auch hinsichtlich der Frage, ob einige oder mehrere dieser Umlenkwalzen angetrieben sind, entsprechen die Umlenkwalzen 24 jenen einer Imprägniervorrichtung des Standes der Technik. Daher wird hier auf eine detailliertere diesbezügliche Erläuterung verzichtet werden.
- In dem dargestellten Ausführungsbeispiel umfasst die Imprägniervorrichtung 10 einen Wannenkörper 26 mit einem Wannenvolumen 26a. In den Wannenkörper 26 ist ein Einsatzkörper 28 eingesetzt, in welchem die erste Teilwanne 18 und die zweite Teilwanne 20 ausgebildet sind. Das vom Einsatzkörper 28 nicht eingenommene Teilvolumen des Wannenvolumens 26a bildet die dritte Teilwanne 22. Erfindungsgemäß ist das Volumen der ersten Teilwanne 18 kleiner als das Volumen der zweiten Teilwanne 20, und Letzteres ist wiederum kleiner als das Volumen der dritten Teilwanne 22.
- Im Betrieb der Imprägniervorrichtung 10 wird der ersten Teilwanne 18 über eine Zulaufleitung 30 Imprägnierflotte 16a zugeführt, die zuvor in einer Erwärmungsvorrichtung 32, vorzugsweise mittels Mikrowellenstrahlung, berührungslos erwärmt worden ist. Der Einlauf der Zulaufleitung 30 in die erste Teilwanne 18 ist bei 34 dargestellt. Erfindungsgemäß kann die Imprägnierflotte 16a etwa 60% Feststoffanteil an Imprägnierharz 16, beispielsweise Melaminharz, in einem Lösungsmittel, beispielsweise Wasser, umfassen und mit einer Temperatur von etwa 50°C bis 80°C in die erste Teilwanne 18 eingeleitet werden. Aufgrund dieser hohen Temperatur verfügt die Imprägnierflotte 16a trotz des hohen Feststoffanteils über eine so niedrige Viskosität, dass sie in der ersten Teilwanne 18 problemlos in die Materialbahn 12 eindringen kann, um diese zu durchtränken. Zur Erleichterung des Eindringens kann die Materialbahn 12 vor Eintritt in die erste Teilwanne 18 mittels einer Sprühvorrichtung 36 befeuchtet und gewünschtenfalls auch vorgewärmt werden.
- Von der ersten Teilwanne 18 gelangt die Imprägnierflotte über einen Überlauf 38 in die zweite Teilwanne 20. Die Begrenzungswandungen 20a der zweiten Teilwandung 20 sind als Wärmetauscherflächen einer Kühleinheit 40 ausgebildet, welche die Imprägnierflotte 16a auf eine Temperatur von etwa 30°C abkühlt, um ihre Standzeit deutlich zu erhöhen. Darüber hinaus wird die Materialbahn 12 in der zweiten Teilwanne 20 nochmals mit Imprägnierflotte 16a getränkt.
- Über einen Überlauf 42 gelangt die Imprägnierflotte 16a von der zweiten Teilwanne 20 in die dritte Teilwanne 22, in welcher eine Tauchstrecke 44 für die Materialbahn 12 vorgesehen ist. Während das eigentliche Durchtränken der Materialbahn 12 mit Imprägnierflotte 16a in den ersten beiden Teilwannen 18 und 20 stattfindet, ist die Hauptfunktion der Tauchstrecke 44 in der dritten Teilwanne 22 sicherzustellen, dass die Materialbahn 12 mit der gewünschten Menge von Imprägnierflotte 16a beladen wird.
- Obgleich in
Fig. 1 an verschiedenen Stellen Rakelstäbe 46 vorgesehen sind, deren Aufgabe es ist, überschüssige Imprägnierflotte 16a von der Oberfläche der Materialbahn 12 abzutragen oder/und die auf die Materialbahn 12 aufgetragene Imprägnierflotte 16a gleichmäßig zu verteilen oder/und zu glätten, befasst sich die vorliegende Erfindung nicht mit diesem Teilaspekt. Daher wird auch diesbezüglich auf eine detailliertere Erläuterung verzichtet werden. - Wie in
Fig. 1 schematisch angedeutet, ist im Boden der Imprägnierwanne 26 eine Kühlvorrichtung 48 vorgesehen, deren Aufgabe es zum einen ist, die Imprägnierflotte 16a im dritten Teilvolumen 22 auf der gewünschten Temperatur von etwa 30°C zu halten, welche im Falle eines Produktionsstillstands zum anderen aber auch dazu genutzt wird, die Imprägnierflotte 16a noch weiter abzukühlen, um ihre Standzeit so weit zu erhöhen, dass sie nach Wiederaufnahme der Produktion verlustfrei weiterverwendet werden kann. Erforderlichenfalls kann hierzu auch noch eine externe Kühlvorrichtung 50 vorgesehen sein, die die Imprägnierflotte 16a aus dem Wannenvolumen 26a umpumpt und kühlt. - Auch im normalen Produktionsbetrieb wird die Imprägnierflotte 16a umgepumpt. Und zwar wird sie über einen Ablauf 52 aus dem Wannenvolumen 26a entnommen und über eine Leitung 54 von einer Pumpe 56 zur Mikrowellen-Erwärmungsvorrichtung 32 und über die Zulaufleitung 30 weiter zum Einlauf 34 in die erste Teilwanne 18 geleitet. Dabei arbeiten die Pumpe 56 und die Mikrowellen-Erwärmungsvorrichtung 32 vorzugsweise unter der Steuerung einer Steuereinheit 58, sodass zum einen sichergestellt ist, dass immer genau die Menge an Imprägnierflotte 16a in die erste Teilwanne 18 eingeleitet wird, die in Abhängigkeit der Produktionsgeschwindigkeit, insbesondere der Laufgeschwindigkeit der Materialbahn 12 benötigt wird, und dass die Imprägnierflotte 16a mit der gewünschten Temperatur in die erste Teilwanne 18 eingeleitet wird.
- Ferner stellt eine Dosiervorrichtung 60 sicher, dass über eine Leitung 62 und einen Zulauf 64 immer genau die Menge an Imprägnierflotte 16 in das Wannenvolumen 26a nachgeliefert wird, die die Materialbahn 12 in Folge des Imprägnierens aus der Imprägniervorrichtung 10 entnimmt. Auf diese Weise kann sichergestellt werden, dass der Spiegel der Imprägnierflotte 16 in den Teilwannen 18, 20 und 22 stets auf der gleichen Höhe gehalten werden kann. Auch die Dosiervorrichtung 60 arbeitet bevorzugt unter der Steuerung der Steuervorrichtung 58.
- Ferner können der Steuervorrichtung 58 die Erfassungssignale einer Mehrzahl von Sensoren S zugeführt werden, beispielsweise eines Sensors zur Erfassung der Geschwindigkeit der Materialbahn 12, eines Sensors zur Erfassung der Temperatur der in die erste Teilwanne 18 eingeleiteten Imprägnierflotte 16a, eines Sensors zur Erfassung des Pegels der Imprägnierflotte 16a in den Teilwannen 18, 20 und 22 und dergleichen Sensoren mehr. Diese Sensoren und ihre Verbindungsleitungen zur Steuervorrichtung 58 sind in
Fig. 1 aus Gründen der Übersichtlichkeit der Darstellung nicht dargestellt. - Nachzutragen ist noch, dass sich die in
Fig. 1 dargestellte Ausführungsform zur Nachrüstung an bereits bestehenden Imprägniervorrichtungen des Standes der Technik eignet. Neben dem Vorsehen einer Mikrowellen-Erwärmungsvorrichtung 32 braucht nämlich lediglich der Einsatzkörper 28, in dem die ersten beiden Teilwannen 18 und 20 ausgebildet sind, in das Wannenvolumen 26a der Imprägnierwanne 26 eingesetzt zu werden, um aus einer Imprägniervorrichtung des Standes der Technik eine erfindungsgemäße Imprägniervorrichtung 10 zu machen. Grundsätzlich ist es jedoch auch möglich, eine speziell hierfür ausgebildete Imprägnierwanne vorzusehen.
Claims (12)
- Vorrichtung (10) zum Imprägnieren bahnförmigen Materials (12) mit wärmehärtbarem Imprägnierharz (16), umfassend:eine Imprägnierwanne (26), in welcher das bahnförmige Material (12) mit dem Imprägnierharz (16) in Kontakt gebracht wird,eine zur Imprägnierwanne (26) führende Zulaufleitung (30), durch welche das Imprägnierharz (16) in die Imprägnierwanne (26) eingeleitet wird,eine Erwärmungsvorrichtung (32), welche das Imprägnierharz (16) erwärmt,dadurch gekennzeichnet, dass die Erwärmungsvorrichtung (32) der Zulaufleitung (30) zugeordnet ist und das Imprägnierharz (16) in der Zulaufleitung (30) erwärmt.
- Vorrichtung nach Anspruch 1,
dadurch gekennzeichnet, dass die Erwärmungsvorrichtung (32) eine berührungslos arbeitende Erwärmungsvorrichtung ist. - Vorrichtung nach Anspruch 1 oder 2,
dadurch gekennzeichnet, dass die Erwärmungsvorrichtung (32) das Imprägnierharz (16) unter Einsatz von Mikrowellenstrahlung erwärmt. - Vorrichtung nach einem der Ansprüche 1 bis 3,
dadurch gekennzeichnet, dass eine Steuervorrichtung (58) vorgesehen ist, welche dafür sorgt, dass der Erwärmungseinrichtung (32) die zum Imprägnieren benötigte Menge an Imprägnierharz (16) zugeführt wird. - Vorrichtung nach einem der Ansprüche 1 bis 4,
dadurch gekennzeichnet, dass die Imprägnierwanne (26) mit einer Kühlvorrichtung (48, 50, 40) versehen ist. - Vorrichtung nach Anspruch 5,
dadurch gekennzeichnet, dass die Kühlvorrichtung (48, 50, 40) eine integrierte Kühleinheit (48) umfasst. - Vorrichtung nach Anspruch 5 oder 6,
dadurch gekennzeichnet, dass die Kühlvorrichtung (48, 50, 40) eine externe Kühleinheit (50) umfasst. - Vorrichtung nach einem der Ansprüche 1 bis 7,
dadurch gekennzeichnet, dass die Imprägnierwanne (26) in wenigstens zwei Teilwannen (18, 20, 22) unterteilt ist. - Vorrichtung nach Anspruch 8,
dadurch gekennzeichnet, dass eine mit der Zulaufleitung (30) verbundene erste Teilwanne (18) ein kleineres Volumen aufweist als eine in Strömungsrichtung des Harzes weiter stromabwärts angeordnete weitere Teilwanne (22). - Vorrichtung nach Anspruch 8 oder 9,
dadurch gekennzeichnet, dass zwischen den beiden Teilwannen (18, 22) eine Kühleinheit (40) angeordnet ist. - Vorrichtung nach einem der Ansprüche 8 bis 10,
dadurch gekennzeichnet, dass wenigstens eine der Teilwannen (18, 20, 22) in einem Wannenkörper (28) ausgebildet ist, der in einen größeren Wannenkörper (26) einsetzbar ist, dessen restliches Wannenvolumen (26ä) wenigstens eine weitere Teilwanne (22) bildet. - Vorrichtung nach einem der Ansprüche 1 bis 11,
dadurch gekennzeichnet, dass eine Sprühvorrichtung (36) vorgesehen ist, welche das bahnförmige Material (12) befeuchtet, beispielsweise mit Wasser, vorzugsweise heißem Wasser oder Wasserdampf.
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL09783817T PL2340332T3 (pl) | 2008-10-07 | 2009-10-07 | Urządzenie do impregnowania materiałów pasmowych termoutwardzalną żywicą impregnacyjną |
| SI200930327T SI2340332T1 (sl) | 2008-10-07 | 2009-10-07 | Naprava za impregnacijo trakasto oblikovanega materiala z impregnirno smolo, ki se trdi na toploti |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102008050704A DE102008050704A1 (de) | 2008-10-07 | 2008-10-07 | Vorrichtung zum Imprägnieren von bahnförmigen Materialien mit wärmehärtbarem Imprägnierharz |
| PCT/EP2009/063040 WO2010040781A2 (de) | 2008-10-07 | 2009-10-07 | Vorrichtung zum imprägnieren von bahnförmigen materialien mit wärmehärtbarem imprägnierharz |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2340332A2 EP2340332A2 (de) | 2011-07-06 |
| EP2340332B1 true EP2340332B1 (de) | 2012-07-25 |
Family
ID=41795137
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP09783817A Not-in-force EP2340332B1 (de) | 2008-10-07 | 2009-10-07 | Vorrichtung zum imprägnieren von bahnförmigen materialien mit wärmehärtbarem imprägnierharz |
Country Status (11)
| Country | Link |
|---|---|
| US (1) | US8945679B2 (de) |
| EP (1) | EP2340332B1 (de) |
| CN (1) | CN102216525B (de) |
| CA (1) | CA2739548C (de) |
| DE (1) | DE102008050704A1 (de) |
| ES (1) | ES2388830T3 (de) |
| PL (1) | PL2340332T3 (de) |
| PT (1) | PT2340332E (de) |
| RU (1) | RU2467115C1 (de) |
| SI (1) | SI2340332T1 (de) |
| WO (1) | WO2010040781A2 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN106676969A (zh) * | 2016-12-28 | 2017-05-17 | 江苏建丰装饰纸有限公司 | 抗菌负氧型液态装饰纸生产工艺 |
Families Citing this family (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3606016A1 (de) | 2011-04-28 | 2020-02-05 | Nokia Technologies Oy | Vorrichtung und verfahren für ein kommunikationsnetz |
| CN102327854B (zh) * | 2011-08-05 | 2013-06-26 | 江苏星源航天材料股份有限公司 | 覆铜板生产润边浸胶方法及装置 |
| CN103395214B (zh) * | 2013-08-06 | 2016-04-13 | 滕州力华米泰克斯胶辊有限公司 | 软压光胶辊覆面材料成型单元设备 |
| CN104985731A (zh) * | 2015-07-02 | 2015-10-21 | 重庆永钢橡塑有限责任公司 | 超长链条自动浸塑设备 |
| JP6927035B2 (ja) * | 2016-02-15 | 2021-08-25 | 東レ株式会社 | イオン伝導膜の製造方法および製造装置 |
| CN208797098U (zh) * | 2018-11-09 | 2019-04-26 | 宁德时代新能源科技股份有限公司 | 极片辊压装置 |
| CN111906882B (zh) * | 2020-08-11 | 2021-10-15 | 曲美家居集团股份有限公司 | 一种家具加工用木板浸漆抹平处理设备 |
| CN112403838A (zh) * | 2020-11-19 | 2021-02-26 | 合肥高地创意科技有限公司 | 一种集成电路保护带表面抗静电液涂覆装置 |
| DE102021001078A1 (de) | 2021-03-01 | 2022-09-01 | Dirk Otto | Vorrichtung und Verfahren zum Herstellen eines Wachs oder eine wachsartige Substanz umfassenden Flächenmaterials, Wundpflaster, Wickel, Wachs-Folie und Frischhaltematerial |
Family Cites Families (26)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2343601A (en) * | 1940-03-09 | 1944-03-07 | Barber Asphalt Corp | Apparatus for saturation of fibrous material |
| US2489456A (en) * | 1945-08-21 | 1949-11-29 | Robert A Liebel | Method of applying uniform coating by immersion |
| US2936733A (en) * | 1958-03-14 | 1960-05-17 | Du Pont | Apparatus for coating |
| FR1244313A (fr) * | 1959-05-06 | 1960-09-19 | Perfectionnement aux traitements mouillés | |
| CH473210A (fr) * | 1967-02-10 | 1969-05-31 | Stadex Ab | Procédé pour l'application d'un revêtement de matière adhésive sur un support et installation pour la mise en oeuvre de ce procédé |
| US3511693A (en) * | 1967-05-01 | 1970-05-12 | Standard Register Co | Hot melt coating |
| US3671298A (en) * | 1970-10-30 | 1972-06-20 | Westvaco Corp | Hydraulic system for controlling resin pickup |
| IL40966A (en) * | 1972-11-29 | 1976-07-30 | Klier S | A process for continuous treatment of textile materials |
| US4051278A (en) * | 1975-06-06 | 1977-09-27 | Eastman Kodak Company | Method for reducing mottle in coating a support with a liquid coating composition |
| GB1604620A (en) * | 1977-11-10 | 1981-12-09 | Britton A | Application of liquid material to webs |
| SU771220A1 (ru) * | 1979-02-26 | 1980-10-15 | Ивановский Ордена Трудового Красного Знамени Текстильный Институт Имени М.В.Фрунзе | Способ заключительной отделки текстильного полотна |
| GB2146673A (en) * | 1983-09-17 | 1985-04-24 | Fordath Ltd | Method of treating a web |
| AT383814B (de) * | 1984-06-22 | 1987-08-25 | Isovolta | Verfahren zum herstellen von mit kunstharz impraegnierten flaechigen traegermaterialien |
| DE4016784A1 (de) * | 1990-05-25 | 1991-11-28 | Werner & Pfleiderer | Extruder zum aufbereiten von kunststoff unter zufuehrung mindestens eines faserstranges |
| DE4129190A1 (de) * | 1991-09-03 | 1993-03-04 | Held Kurt | Verfahren und vorrichtung zur kontinuierlichen herstellung von harzimpraegnierten materialbahnen |
| FI95061C (fi) * | 1993-03-08 | 1995-12-11 | Valmet Paper Machinery Inc | Menetelmä paperiradan kalanteroinnissa ja menetelmää soveltava kalanteri |
| DE29501919U1 (de) | 1995-02-07 | 1995-04-06 | Vits Maschinenbau GmbH, 40764 Langenfeld | Vorrichtung zum Imprägnieren von Bahnen aus porösem Material |
| RU2157868C2 (ru) * | 1998-11-10 | 2000-10-20 | Общество с ограниченной ответственностью "Технобум" | Устройство для пропитки движущегося полотна, преимущественно целлюлозного |
| DE19937467A1 (de) * | 1999-08-07 | 2001-02-08 | Roland Man Druckmasch | Vorrichtung zum Temperieren von Beschichtungsmedien |
| DE10114708A1 (de) * | 2001-03-26 | 2002-10-24 | Klaus-Kurt Koelzer | Verstärkungsmaterial mit volumisierten Fasern |
| FI115850B (fi) * | 2002-04-10 | 2005-07-29 | Metso Paper Inc | Menetelmä ja laite aineen siirtämiseksi rainaan |
| US7704544B2 (en) * | 2003-10-07 | 2010-04-27 | Advanced Cardiovascular Systems, Inc. | System and method for coating a tubular implantable medical device |
| ITMI20040804A1 (it) * | 2004-04-23 | 2004-07-23 | Tocchio S R L | Metodo ed apparecchiatura per la realizzazione di carte decorative e di pannelli laminati incorporanti tali carte decorative in particolare carte decorative e pannelli di copertura di superfici di pavimentazione mobili o pareti |
| RU2291885C2 (ru) * | 2004-08-16 | 2007-01-20 | Валентина Константиновна Комарова | Электроизоляционный материал |
| US7845308B1 (en) * | 2005-10-26 | 2010-12-07 | Lam Research Corporation | Systems incorporating microwave heaters within fluid supply lines of substrate processing chambers and methods for use of such systems |
| DE102008032053A1 (de) * | 2008-07-08 | 2010-01-14 | Kaindl Decor Gmbh | Verfahren und Vorrichtung zum Trocknen und Vorkondensieren von Imprägnaten, welche aus mit Kunstharz getränktem, folienartigem Bahnmaterial gebildet sind; Melaminharz-freies Imprägnat |
-
2008
- 2008-10-07 DE DE102008050704A patent/DE102008050704A1/de not_active Withdrawn
-
2009
- 2009-10-07 US US13/122,891 patent/US8945679B2/en not_active Expired - Fee Related
- 2009-10-07 ES ES09783817T patent/ES2388830T3/es active Active
- 2009-10-07 CN CN2009801455904A patent/CN102216525B/zh not_active Expired - Fee Related
- 2009-10-07 RU RU2011117347/05A patent/RU2467115C1/ru not_active IP Right Cessation
- 2009-10-07 SI SI200930327T patent/SI2340332T1/sl unknown
- 2009-10-07 PL PL09783817T patent/PL2340332T3/pl unknown
- 2009-10-07 WO PCT/EP2009/063040 patent/WO2010040781A2/de not_active Ceased
- 2009-10-07 CA CA2739548A patent/CA2739548C/en not_active Expired - Fee Related
- 2009-10-07 PT PT09783817T patent/PT2340332E/pt unknown
- 2009-10-07 EP EP09783817A patent/EP2340332B1/de not_active Not-in-force
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN106676969A (zh) * | 2016-12-28 | 2017-05-17 | 江苏建丰装饰纸有限公司 | 抗菌负氧型液态装饰纸生产工艺 |
| CN106676969B (zh) * | 2016-12-28 | 2019-01-11 | 江苏建丰装饰纸有限公司 | 抗菌负氧型液态装饰纸生产工艺 |
Also Published As
| Publication number | Publication date |
|---|---|
| PL2340332T3 (pl) | 2012-10-31 |
| CA2739548C (en) | 2017-07-04 |
| US8945679B2 (en) | 2015-02-03 |
| WO2010040781A3 (de) | 2011-03-10 |
| SI2340332T1 (sl) | 2012-12-31 |
| US20110290180A1 (en) | 2011-12-01 |
| CN102216525B (zh) | 2013-11-06 |
| CA2739548A1 (en) | 2010-04-15 |
| PT2340332E (pt) | 2012-08-29 |
| CN102216525A (zh) | 2011-10-12 |
| RU2467115C1 (ru) | 2012-11-20 |
| DE102008050704A1 (de) | 2010-04-08 |
| ES2388830T3 (es) | 2012-10-19 |
| EP2340332A2 (de) | 2011-07-06 |
| WO2010040781A2 (de) | 2010-04-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2340332A2 (de) | Vorrichtung zum imprägnieren von bahnförmigen materialien mit wärmehärtbarem imprägnierharz | |
| EP1571249B1 (de) | Vorrichtung und Verfahren zum Aufbringen von Avivagen auf eine Vliesbahn | |
| EP3504051B1 (de) | Vorrichtung und verfahren zur imprägnierung von faserstrukturen | |
| DE112007001442B4 (de) | Verfahren und Vorrichtung zur Behandlung einer Faserbahn | |
| DE102010052044A1 (de) | Verfahren und Anlage zum Imprägnieren und Trocknen einer durchlaufenden Papierbahn | |
| EP0624665A2 (de) | Verfahren und Vorrichtung zur Herstellung von Fasern nach einem Zentrifugalspinnverfahren | |
| WO2013160290A1 (de) | Verfahren und rakelvorrichtung zum aufrakeln einer harzpaste auf eine trägerfolie und eine harzmattenanlage zur herstellung von harzmatten | |
| EP0591287B1 (de) | Verfahren zum imprägnieren eines flächigen, faserigen trägermaterials mit kunstharz, sowie vorrichtungen zur durchführung dieses verfahrens | |
| EP2844797B1 (de) | Verfahren zum beschichten einer papierbahn | |
| DE102008032053A1 (de) | Verfahren und Vorrichtung zum Trocknen und Vorkondensieren von Imprägnaten, welche aus mit Kunstharz getränktem, folienartigem Bahnmaterial gebildet sind; Melaminharz-freies Imprägnat | |
| EP3239397B1 (de) | Verfahren und anlage zum herstellen eines flächigen imprägnierten faserstoffproduktes | |
| DE2729219C2 (de) | Verfahren und Vorrichtung zur kontinuierlichen Herstellung von faserverstärkten Bahnen aus Kunstharz (Prepregs) mit Gelcoat-Deckschicht | |
| DE3817800A1 (de) | Verfahren und anlage zur herstellung einer faserverstaerkten bahn aus kunstharz, insbesondere von prepreg | |
| DE3114592C2 (de) | Auftrags- und Dosiereinrichtung, insbesondere für Doppelbandpressen | |
| EP2186635B1 (de) | Verfahren zum Beschichten von Holzwerkstoffplatten mit einer Verschleißschicht und dadurch hergestellte Holzwerkstoffplatten | |
| DE2404604A1 (de) | Vorrichtung und verfahren zum behandeln einer kontinuierlich vorwaerts bewegten materialbahn mit einem fluid | |
| DE102006052136B4 (de) | Verfahren und Vorrichtung zur kontinuierlichen Herstellung von Prepregs | |
| DE102004005087A1 (de) | Tragbalken | |
| EP2596165A1 (de) | Vorrichtung zum auftragen von fluiden medien | |
| EP1733802A1 (de) | Vorrichtung zum Auftragen von flüssigen bis pastösen Suspensionen auf Papier- oder Kartonbahnen | |
| EP4488066A1 (de) | Verfahren und vorrichtung zum bedrucken eines plattenförmigen werkstückes | |
| DE102007027817A1 (de) | Rakelvorrichtung | |
| DE2224881A1 (de) | Vorrichtung zum trocknen, vergueten oder haerten eines kunststoffharzes und dgl | |
| DE102005005162A1 (de) | Verfahren und Vorrichtung zur Herstellung von Laminaten | |
| DE202004021046U1 (de) | Tragbalken |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20110407 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA RS |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 567783 Country of ref document: AT Kind code of ref document: T Effective date: 20120815 Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20120823 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502009004197 Country of ref document: DE Effective date: 20120920 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2388830 Country of ref document: ES Kind code of ref document: T3 Effective date: 20121019 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: T3 Ref document number: E 12271 Country of ref document: SK |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D Effective date: 20120725 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20121025 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20121125 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20121026 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 |
|
| 26 | Opposition filed |
Opponent name: VITS TECHNOLOGY GMBH Effective date: 20130424 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121031 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R026 Ref document number: 502009004197 Country of ref document: DE Effective date: 20130424 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20121025 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121007 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R100 Ref document number: 502009004197 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 |
|
| PLCK | Communication despatched that opposition was rejected |
Free format text: ORIGINAL CODE: EPIDOSNREJ1 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091007 |
|
| PLBN | Opposition rejected |
Free format text: ORIGINAL CODE: 0009273 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION REJECTED |
|
| 27O | Opposition rejected |
Effective date: 20140515 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R100 Ref document number: 502009004197 Country of ref document: DE Effective date: 20140515 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120725 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SK Payment date: 20190924 Year of fee payment: 11 Ref country code: RO Payment date: 20190923 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20191021 Year of fee payment: 11 Ref country code: PL Payment date: 20190925 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20191004 Year of fee payment: 11 Ref country code: NL Payment date: 20191021 Year of fee payment: 11 Ref country code: DE Payment date: 20190731 Year of fee payment: 11 Ref country code: PT Payment date: 20191003 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20191028 Year of fee payment: 11 Ref country code: SI Payment date: 20190918 Year of fee payment: 11 Ref country code: BE Payment date: 20191021 Year of fee payment: 11 Ref country code: IT Payment date: 20191028 Year of fee payment: 11 Ref country code: ES Payment date: 20191122 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20191021 Year of fee payment: 11 Ref country code: TR Payment date: 20191001 Year of fee payment: 11 Ref country code: AT Payment date: 20191022 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20191021 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502009004197 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20201101 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 567783 Country of ref document: AT Kind code of ref document: T Effective date: 20201007 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20201007 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: MM4A Ref document number: E 12271 Country of ref document: SK Effective date: 20201007 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20201031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201101 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210501 Ref country code: SK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210407 Ref country code: RO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201008 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 |
|
| REG | Reference to a national code |
Ref country code: SI Ref legal event code: KO00 Effective date: 20210811 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20220120 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201007 |