EP1855824B1 - Verfahren zum herstellen einer stranggiesskokille und stranggiesskokille - Google Patents
Verfahren zum herstellen einer stranggiesskokille und stranggiesskokille Download PDFInfo
- Publication number
- EP1855824B1 EP1855824B1 EP06723315.5A EP06723315A EP1855824B1 EP 1855824 B1 EP1855824 B1 EP 1855824B1 EP 06723315 A EP06723315 A EP 06723315A EP 1855824 B1 EP1855824 B1 EP 1855824B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- casting
- mold
- continuous casting
- waves
- casting direction
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/04—Continuous casting of metals, i.e. casting in indefinite lengths into open-ended moulds
- B22D11/057—Manufacturing or calibrating the moulds
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T409/00—Gear cutting, milling, or planing
- Y10T409/30—Milling
- Y10T409/303752—Process
Definitions
- the invention relates to a method for producing a continuous casting mold in which at least one surface is mechanically processed which, when the mold is used as intended, is in contact with molten material.
- the invention also relates to a continuous casting mold.
- Continuous casting molds which are characterized by a special surface design in order, in particular, to influence the heat transfer from the steel into the mold wall in a favorable manner.
- the EP 1 099 496 A1 provides for mold plates to be completely or partially provided with a surface texture in order to reduce the heat flow.
- the texture is preferably produced by sandblasting or shot peening after the mechanical processing. This makes it possible to increase the roughness of that surface of the mold which, when the continuous casting mold is used as intended, is in contact with molten material.
- JP 10 193 042 A a continuous casting mold is described, wherein longitudinal grooves are deliberately introduced into the surface of the broadside plates. The aim of this is to reduce the heat flow density in the meniscus in order to avoid longitudinal cracks.
- a continuous casting mold is known in which a reduction in the heat flow density is sought, namely in the upper region of the mold. This is achieved by increasing the wall thickness of the mold in its upper area or by using more insulating material in this area.
- the upper part of the mold can either consist entirely of this material or be coated with this material on the water side.
- the FR 2 658 440 describes a continuous casting mold in which a local reduction in the heat flux density is achieved by making grooves in the hot side of the mold and filling these grooves with a second material with low thermal conductivity. In addition, the entire surface of the mold is coated with this second material.
- JP 06 134 553 A and in the JP 03 128 149 A describes the roughening of the surface of casting rollers, which is intended to reduce the heat flux density in this application.
- EP-A-1 099 496 A1 a method for producing a continuous casting mold according to the preamble of claim 1 and such a continuous casting mold according to the preamble of claim 2 are known.
- a continuous casting mold for casting strands of metal the casting cross-section of which is delimited by plates made of copper alloys, which form broad-side plates or narrow-side plates, with a surface that is arranged at least in the bath mirror area on the hot side and formed against wear and heat, and at least in the broad side plates in the bath mirror area a recessed, strip-shaped mold section is provided, and the recessed surface is given a greater surface roughness by a blasting process, is off DE-A 102 56 751 known.
- the thickness and the structure of the casting powder layer between the mold wall and the strand shell largely determine the level of heat flow density between the steel and the mold and thus the thermal load on both the strand shell and the mold material. Due to local and temporal changes in the casting powder layer, especially in the area of the casting level, strong stresses can arise in the strand shell, which lead to longitudinal cracks, especially in the case of steel types that are sensitive to cracks. However, the surface of the mold is also exposed to strong mechanical loads as a result of changing thermal loads. Therefore, the maximum heat flow in the area of the meniscus should be low and as uniform as possible in order to reduce the risk of cracking, especially in the case of steel types that are sensitive to longitudinal cracks.
- the aim is that the friction between the broad sides and the narrow sides of the mold is as low as possible during the narrow side adjustment.
- the aim is to reduce the thermal load in the meniscus through a low heat flux density, which should have a positive effect on the life of the mold.
- the invention is therefore based on the object of creating a method for producing a continuous casting mold and a continuous casting mold with which the stated desired properties are achieved as well as possible, this being achieved with the least possible manufacturing effort and thus with low costs.
- the solution to this problem by the invention is characterized according to the method that as the last work step in the production of the surface of Mold a mechanical processing is carried out, which generates an anisotropically structured surface, in such a way that the surface of the mold has a greater roughness in the casting direction than in the direction transverse to the casting direction and has elevations and depressions formed in lines and oriented transversely to the casting direction
- the last step is a milling process.
- Anisotropy is understood to mean that surface characteristics change depending on the surface direction in which they are determined. In the case of the surface of the mold in question here, this means in particular that parameters such as B. measured roughness in the casting direction have different values than perpendicular to it, d. H. in the transverse direction to the casting direction.
- the continuous casting mold which has at least one mechanically processed surface which, when used as intended, is in contact with molten material, is characterized according to the invention in that the surface at least partially has an anisotropic structure such that the surface of the mold has a greater roughness in the casting direction than in the direction transverse to the casting direction, and that the surface has elevations and depressions which are linearly designed and oriented and which run in the direction transverse to the casting direction, the elevations and depressions being designed as waves whose wave crests and troughs extend in the direction transverse to the casting direction, the height of the waves is between 2 ⁇ m and 250 ⁇ m.
- the anisotropically structured surface has line-shaped and oriented elevations and depressions which run in the direction transverse to the casting direction, these elevations and depressions are designed as waves, the wave crests and troughs of which extend in the direction transverse to the casting direction (G); the shafts preferably have a substantially rounded shape in cross section. It has proven useful if the height of the waves is between 2 ⁇ m and 250 ⁇ m, in particular between 10 ⁇ m and 50 ⁇ m.
- the height of the waves on the surface can remain constant in the casting direction and / or transversely to the casting direction or can be set variably.
- the proposal of the invention is therefore based on the fact that the desired anisotropic surface structure is produced in the last step of the shaping, mechanical processing of the mold surface.
- the machined surface is advantageously designed in such a way that it is different in the casting direction macroscopic structure is generated as being transverse to the casting direction. Equally, the microscopic roughness of the surface can also be designed differently in the casting direction and across it.
- both the increased roughness and the macroscopic structure of the surface lead to a reduction and equalization of the heat flow, which also leads to a reduction in the tendency towards longitudinal cracks.
- the thermal load on the mold plate is also reduced, which results in a longer service life of the mold plates.
- the desired surface structure is created during the mechanical, machining of the mold surface.
- further processing steps such as B. the introduction of grooves in the surface, the coating of the surface in the meniscus area or the roughening of the surface by sand or shot peening, are not required, which makes the inventive proposal economical.
- the advantageous anisotropic surface structure can be produced without great effort not only during the production of the molds, but also each time the mold surface is reworked, which has to take place at certain time intervals.
- molds that consist of individual mold plates (e.g. slab, thin slab) additionally the friction between wide and narrow sides when adjusting the narrow sides is also reduced.
- Fig. 1 the view of that surface of a mold plate of a continuous casting mold 1 is shown which, when the continuous casting mold 1 is in use, is in contact with molten material (steel) or the solidified strand shell.
- the strand shell passes the mold plate in the casting direction G.
- the surface 2 is provided with a special structure:
- the surface topology, in particular the roughness, of the surface 2 is anisotropic, ie it results in the casting direction G and different roughness values in direction Q transverse to casting direction G.
- the mold plate is provided with a large number of elevations and depressions, which in Fig. 1 are only shown very schematically.
- the production of these elevations and depressions takes place during the last mechanical processing operation in the production of the mold plate.
- the surface of the mold plate is milled using the line milling process.
- z. B. used a milling tool with a diameter of 100 to 150 mm, which with conventional indexable inserts, z. B. made of hard metal is provided.
- the material consumption in the last processing step is lower than 1 mm, preferably less than 0.5 mm.
- the characteristics and structure of the elevations and depressions on the mold surface can be specifically set.
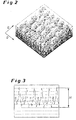
- Fig. 2 shows the profile of the finished surface in three-dimensional view. It can be seen here that the roughness of the surface in the casting direction G is greater than that transversely to the casting direction Q.
- the mold plate is thus provided with a large number of elevations and depressions, which are shown in FIG Fig. 1 are only shown very schematically. The production of these elevations and depressions takes place during the last mechanical processing operation in the production of the mold plate.
- the height H of the line-shaped oriented elevations and depressions is in Fig. 3 can be seen and is typically in the range from 2 ⁇ m to 250 ⁇ m, which can be influenced by the choice of milling parameters.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Continuous Casting (AREA)
Description
- Die Erfindung betrifft ein Verfahren zum Herstellen einer Stranggießkokille, bei der zumindest eine Oberfläche mechanisch bearbeitet wird, die bei der bestimmungsgemäßen Benutzung der Kokille Kontakt mit schmelzflüssigem Material hat. Des Weiteren betrifft die Erfindung eine Stranggießkokille.
- Es sind Stranggießkokillen bekannt, die sich durch eine spezielle Oberflächenausgestaltung auszeichnen, um insbesondere den Wärmeübergang vom Stahl in die Kokillenwand in einer günstigen Weise zu beeinflussen.
- Die
EP 1 099 496 A1 sieht vor, zur Reduzierung des Wärmestroms Kokillenplatten ganz oder teilweise mit einer Oberflächentextur zu versehen. Die Textur wird dabei im Anschluss an die mechanische Bearbeitung vorzugsweise durch Sand- oder Kugelstrahlen erzeugt. Hierdurch kann die Rauheit derjenigen Oberfläche der Kokille erhöht werden, die bei bestimmungsgemäßem Gebrauch der Stranggießkokille Kontakt zu schmelzflüssigem Material hat. - In der
JP 10 193 042 A - Aus der
JP 02 020 645 A - Aus der
AT 269 392 - Die
FR 2 658 440 - In der
JP 06 134 553 A JP 03 128 149 A - Aus
EP-A-1 099 496 A1 - Eine Stranggießkokille zum Gießen von Strängen aus Metall,deren Gießquerschnitt durch Platten aus Kupferlegierungen begrenzt ist, die Breitseitenplatten oder Schmalseitenplatten bilden, wobei eine zumindest im Badspiegelbereich auf der Heißseite angeordnete, gegen Verschleiß und Hitze gebildete Oberfläche vorgesehen ist, wobei zumindest in den Breitseitenplatten im Badspiegelbereich ein vertiefter, streifenförmiger Kokillenabschnitt vorgesehen ist, und die vertiefte Oberfläche durch ein Strahlverfahren eine größere Rauhtiefe erhält, ist aus
DE-A 102 56 751 bekannt. - Aus
DE-A 19 919 777 ist es bekannt, für Platten aus Kupferlegierungen im Anschluss an eine mechanische Bearbeitung stets ein Glattwalzen durchzuführen, so dass damit eine Stranggießkokille, die aus solchen Platten hergestellt wird, an ihrer Arbeitsseite eine äußerst glatte Oberflächenstruktur mit sehr geringen Rauhtiefen von nur etwa 0,8 µm erhält,
Mit den vorbekannten Maßnahmen soll ein verbessertes thermodynamisches Verhalten der Kokille und insbesondere deren Wandungen sowie eine verbesserte Einsatzfähigkeit beim Stranggießen erreicht werden. Generell wird eine gute Haftung des Gießpulvers an der Kokillenplatte und eine gleichmäßige Verteilung des Wärmestroms über die gesamte Kokille angestrebt. - Die Dicke und die Struktur der Gießpulverschicht zwischen der Kokillenwand und der Strangschale bestimmt maßgeblich die Höhe der Wärmestromdichte zwischen Stahl und Kokille und damit die thermische Belastung sowohl der Strangschale als auch des Kokillenmaterials. Durch lokale und zeitliche Änderungen der Gießpulverschicht besonders im Bereich des Gießspiegels können deshalb starke Spannungen in der Strangschale entstehen, die besonders bei rissempfindlichen Stahlsorten zu Längsrissen führen. Aber auch die Oberfläche der Kokille wird durch wechselnde thermische Beaufschlagung starken mechanischen Belastungen ausgesetzt. Daher soll der maximale Wärmestrom im Bereich des Gießspiegels niedrig und möglichst gleichmäßig sein, um so besonders bei längsrissempfindlichen Stahlsorten die Gefahr der Rissbildung zu verringern.
- Zusätzlich wird angestrebt, dass die Reibung zwischen den Breitseiten und den Schmalseiten der Kokille während der Schmalseitenverstellung möglichst gering ist. Schließlich wird angestrebt, dass durch eine geringe Wärmestromdichte die thermische Belastung im Gießspiegel verringert wird, was sich positiv auf die Lebensdauer der Kokille auswirken soll.
- Die vorgeschlagenen Maßnahmen erreichen dieses Ziel nur teilweise bzw. mit einem relativ hohen Fertigungsaufwand.
- Der Erfindung liegt daher die Aufgabe zugrunde, ein Verfahren zur Herstellung einer Stranggießkokille sowie eine Stranggießkokille zu schaffen, mit dem bzw. mit der die genannten angestrebten Eigenschaften möglichst gut erreicht werden, wobei dies mit möglichst geringem Fertigungsaufwand und damit mit geringen Kosten erreicht werden soll.
- Die Lösung dieser Aufgabe durch die Erfindung ist verfahrensgemäß dadurch gekennzeichnet, dass als letzter Arbeitsschritt bei der Herstellung der Oberfläche der Kokille eine mechanische Bearbeitung durchgeführt wird, die eine anisotrop strukturierte Oberfläche erzeugt, derart, dass die Oberfläche der Kokille in Gießrichtung eine größere Rauheit aufweist als in Richtung quer zur Gießrichtung und zeilenförmig ausgebildete und orientierte Erhöhungen und Vertiefungen aufweist, die in Richtung quer zur Gießrichtung verlaufen, wobei der letzte Arbeitsschritt ein Fräsverfahren ist.
- Unter Anisotropie ist zu verstehen, dass sich Oberflächencharakteristika in Abhängigkeit der Oberflächenrichtung ändern, in denen sie bestimmt werden. Bei der hier in Rede stehenden Oberfläche der Kokille heißt dies insbesondere, dass Parameter wie z. B. Rauheit in Gießrichtung gemessen andere Werte aufweisen, als senkrecht dazu, d. h. in Querrichtung zur Gießrichtung.
- Die Stranggießkokille, die zumindest eine mechanisch bearbeitete Oberfläche aufweist, die bei ihrer bestimmungsgemäßen Benutzung Kontakt mit schmelzflüssigem Material hat, ist erfindungsgemäß dadurch gekennzeichnet, dass die Oberfläche zumindest teilweise eine anisotrope Struktur aufweist, derart, dass die Oberfläche der Kokille in Gießrichtung eine größere Rauheit aufweist als in Richtung quer zur Gießrichtung, und dass die Oberfläche zeilenförmig ausgebildete und orientierte Erhöhungen und Vertiefungen aufweist, die in Richtung quer zur Gießrichtung verlaufen, wobei die Erhöhungen und Vertiefungen als Wellen ausgebildet sind, deren Wellenberge und Wellentäler in Richtung quer zur Gießrichtung verlaufen, und die Höhe der Wellen zwischen 2 µm und 250 µm beträgt.
- Unter Berücksichtigung dessen, dass die anisotrop strukturierte Oberfläche zeilenförmig ausgebildete und orientierte Erhöhungen und Vertiefungen aufweist, die in Richtung quer zur Gießrichtung verlaufen, sind diese Erhöhungen und Vertiefungen als Wellen ausgebildet, deren Wellenberge und Wellentäler in Richtung quer zur Gießrichtung (G) verlaufen; die Wellen haben dabei vorzugsweise im Querschnitt im Wesentlichen eine abgerundete Form. Bewährt hat es sich, wenn die Höhe der Wellen zwischen 2 µm und 250 µm, insbesondere zwischen 10 µm und 50 µm, beträgt.
- Die Höhe der Wellen auf der Oberfläche kann in Gießrichtung und/oder quer zur Gießrichtung konstant bleiben oder variabel eingestellt werden.
- Der Erfindungsvorschlag stellt also darauf ab, dass die gewünschte anisotrope Oberflächenstruktur im letzten Schritt der formgebenden, mechanischen Bearbeitung der Kokillenoberfläche erzeugt wird. Vorteilhaft wird dabei die bearbeitete Oberfläche so gestaltet, dass in Gießrichtung eine andere makroskopische Struktur erzeugt wird als quer zur Gießrichtung. Gleichermaßen kann auch die mikroskopische Rauheit der Oberfläche in Gießrichtung und quer dazu unterschiedlich ausgebildet sein.
- Mit einer größeren Rauheit in Gießrichtung sowie einer makroskopischen Struktur der Oberfläche mit zeilenförmig quer zur Gießrichtung verlaufenden Erhöhungen wird erreicht, dass die Gießpulverschicht besonders im Bereich des Gießspiegels besser an der Kokillenplatte haftet und nicht so leicht vom Strang - vollständig oder nur lokal - abgerieben wird. Gleichzeitig kommt es sowohl durch die erhöhte Rauheit als auch durch die makroskopische Struktur der Oberfläche zu einer Reduktion und Vergleichmäßigung des Wärmestroms, was ebenfalls zu einer Verringerung der Längsrissneigung führt. Durch die Reduzierung der Wärmestromdichte im Gießspiegel wird zusätzlich die thermische Belastung der Kokillenplatte verringert, was eine höhere Standzeit der Kokillenplatten zur Folge hat.
- Von Vorteil ist es weiterhin, dass die gewünschte Oberflächenstruktur während der mechanischen, spanabhebenden Bearbeitung der Kokillenoberfläche entsteht. Das bedeutet, dass weitere Bearbeitungsschritte, wie z. B. das Einbringen von Nuten in die Oberfläche, das Beschichten der Oberfläche im Gießspiegelbereich oder das Aufrauen der Oberfläche durch Sand- oder Kugelstrahlen, nicht erforderlich sind, was den Erfindungsvorschlag wirtschaftlich macht. Damit kann die vorteilhafte anisotrope Oberflächenstruktur ohne großen Aufwand nicht nur bei der Fertigung der Kokillen, sondern auch bei jeder Überarbeitung der Kokillenoberfläche erzeugt werden, was in gewissen zeitlichen Abständen zu erfolgen hat.
- Durch die Gestaltung der Kokillenoberflächen in der beschriebenen Weise mit quer zur Gießrichtung orientierten makroskopischen Erhöhungen bzw. durch eine Rauheit, die in Gießrichtung größer ist als quer zu ihr, wird bei Kokillen, die aus einzelnen Kokillenplatten bestehen (z. B. Bramme, Dünnbramme) zusätzlich auch die Reibung zwischen Breit- und Schmalseiten bei der Schmalseitenverstellung reduziert.
- In der Zeichnung ist ein Ausführungsbeispiel der Erfindung dargestellt.
- Es zeigen:
- Fig. 1
- schematisch eine Kokillenplatte mit anisotroper Oberfläche sowie die Oberflächentopologie in vergrößerter Darstellung,
- Fig. 2
- schematisch das Profil der Oberfläche der Kokillenplatte in dreidimensionaler Darstellung und
- Fig. 3
- den vergrößert dargestellten Schnitt A-B gemäß
Fig. 1 . - In
Fig. 1 ist die Ansicht derjenigen Fläche einer Kokillenplatte einer Stranggießkokille 1 dargestellt, die im Einsatz der Stranggießkokille 1 mit schmelzflüssigem Material (Stahl) bzw. der erstarrten Strangschale Kontakt hat. Die Strangschale passiert dabei die Kokillenplatte in Gießrichtung G. Damit die oben erläuterten Vorteile erzielt werden, ist die Oberfläche 2 mit einer speziellen Struktur versehen: Die Oberflächentopologie, insbesondere die Rauhigkeit, der Oberfläche 2 ist anisotrop ausgebildet, d. h. es ergeben sich in Gießrichtung G und in Richtung Q quer zur Gießrichtung G unterschiedliche Rauhigkeitswerte. - Die Kokillenplatte ist hierbei mit einer Vielzahl von Erhöhungen und Vertiefungen versehen, die in
Fig. 1 nur sehr schematisch dargestellt sind. Die Herstellung dieser Erhöhungen und Vertiefungen erfolgt beim letzten mechanischen Bearbeitungsvorgang bei der Fertigung der Kokillenplatte. Die Oberfläche der Kokillenplatte wird im letzten Bearbeitungsschritt im Zeilenfräsverfahren gefräst. Hierzu wird z. B. ein Fräswerkzeug mit einem Durchmesser von 100 bis 150 mm eingesetzt, das mit üblichen Wendeschneidplatten, z. B. aus Hartmetall, versehen ist. Die Materialabnahme beim letzten Bearbeitungsschritt ist gegeringer als 1 mm, vorzugsweise geringer als 0,5 mm. Entsprechend der gewählten Abnahme sowie der weiteren Fräsparameter wie Drehzahl, Vorschubgeschwindigkeit, Schnittgeschwindigkeit, Abstand der gefrästen Zeilen, Kühlmittel, Fräsrichtung sowie Anstellwinkel des Werkzeugs zur Plattenoberfläche (Sturz), lassen sich Ausprägungen und Struktur der Erhöhungen und Vertiefungen auf der Kokillenoberfläche gezielt einstellen. -
Fig. 2 zeigt das Profil der endbearbeiteten Oberfläche in dreidimensionaler Ansicht. Hier wird ersichtlich, dass die Rauheit der Oberfläche in Gießrichtung G größer ist als quer zur Gießrichtung Q. Die Kokillenplatte ist also mit einer Vielzahl von Erhebungen und Vertiefungen versehen, die inFig. 1 nur sehr schematisch dargestellt sind. Die Herstellung dieser Erhebungen und Vertiefungen erfolgt beim letzten mechanischen Bearbeitungsvorgang bei der Fertigung der Kokillenplatte. - Die Höhe H der zeilenförmig orientierten Erhöhungen und Vertiefungen ist in
Fig. 3 zu sehen und liegt typischerweise im Bereich von 2 µm bis 250 µm, was durch die Wahl der Fräsparameter beeinflusst werden kann. -
- 1
- Stranggießkokille
- 2
- Oberfläche
- 3
- Wellenstruktur
- G
- Gießrichtung
- Q
- Richtung quer zur Gießrichtung
- H
- Höhe der Wellen
Claims (5)
- Verfahren zum Herstellen einer Stranggießkokille (1), bei der zumindest eine Oberfläche (2) mechanisch bearbeitet wird, die bei der bestimmungsgemäßen Benutzung der Kokille Kontakt mit schmelzflüssigem Material hat,
dadurch gekennzeichnet,
dass im letzten Arbeitsschritt bei der Herstellung der Oberfläche (2) der Kokille (1) eine mechanische Bearbeitung durchgeführt wird, die eine anisotrop strukturierte Oberfläche erzeugt, derart, dass die Oberfläche (2) der Kokille (1) in Gießrichtung (G) eine größere Rauheit aufweist als in Richtung (Q) quer zur Gießrichtung (G) und zeilenförmig ausgebildete und orientierte Erhöhungen und Vertiefungen aufweist, die in Richtung (Q) quer zur Gießrichtung (G) verlaufen und als Wellen ausgebildet sind, deren Wellenberge und Wellentäler in Richtung (Q) quer zur Gießrichtung (G) verlaufen, wobei die Höhe der Wellen zwischen 2 µm und 250 µm beträgt, und
dass der letzte Arbeitsschritt ein Fräsverfahren ist. - Stranggießkokille (1), die zumindest eine mechanisch bearbeitete Oberfläche (2) aufweist, die bei ihrer bestimmungsgemäßen Benutzung Kontakt mit schmelzflüssigem Material hat, hergestellt nach dem Verfahren nach Anspruch 1,
dadurch gekennzeichnet,
dass die Oberfläche (2) zumindest teilweise eine anisotrope Struktur aufweist, derart, dass die Oberfläche (2) der Kokille (1) in Gießrichtung (G) eine größere Rauheit aufweist als in Richtung (Q) quer zur Gießrichtung (G),
dass die Oberfläche (2) zeilenförmig ausgebildete und orientierte Erhöhungen und Vertiefungen aufweist, die in Richtung (Q) quer zur Gießrichtung (G) verlaufen, wobei die Erhöhungen und Vertiefungen als Wellen ausgebildet sind, deren Wellenberge und Wellentäler in Richtung (Q) quer zur Gießrichtung (G) verlaufen, und
dass die Höhe (H) der Wellen zwischen 2 µm und 250 µm beträgt. - Stranggießkokille nach Anspruch 2,
dadurch gekennzeichnet,
dass die Wellen im Querschnitt im Wesentlichen eine abgerundete Form aufweisen. - Stranggießkokille nach Anspruch 2 oder 3,
dadurch gekennzeichnet,
dass die Höhe (H) der Wellen in Gießrichtung (G) konstant ist. - Stranggießkokille nach Anspruch 2 oder 3,
dadurch gekennzeichnet,
dass die Höhe (H) der Wellen in Gießrichtung (G) variabel ist.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102005011532 | 2005-03-10 | ||
| DE102005023745.2A DE102005023745B4 (de) | 2005-03-10 | 2005-05-24 | Verfahren zum Herstellen einer Stranggiesskokille und Stranggiesskokille |
| PCT/EP2006/002164 WO2006094803A1 (de) | 2005-03-10 | 2006-03-09 | Verfahren zum herstellen einer stranggiesskokille und stranggiesskokille |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1855824A1 EP1855824A1 (de) | 2007-11-21 |
| EP1855824B1 true EP1855824B1 (de) | 2021-02-17 |
Family
ID=36266231
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP06723315.5A Expired - Lifetime EP1855824B1 (de) | 2005-03-10 | 2006-03-09 | Verfahren zum herstellen einer stranggiesskokille und stranggiesskokille |
Country Status (8)
| Country | Link |
|---|---|
| US (2) | US20080173422A1 (de) |
| EP (1) | EP1855824B1 (de) |
| JP (1) | JP4559520B2 (de) |
| KR (1) | KR101152678B1 (de) |
| CN (1) | CN101137453B (de) |
| CA (1) | CA2597100C (de) |
| ES (1) | ES2864578T3 (de) |
| WO (1) | WO2006094803A1 (de) |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5606824B2 (ja) * | 2010-08-18 | 2014-10-15 | 株式会社不二製作所 | 金型の表面処理方法及び前記方法で表面処理された金型 |
| DE102013114326A1 (de) * | 2013-12-18 | 2015-06-18 | Thyssenkrupp Steel Europe Ag | Gießkokille zum Vergießen von Stahlschmelze |
| JP6413991B2 (ja) * | 2015-09-14 | 2018-10-31 | Jfeスチール株式会社 | スラブの表面手入れ方法 |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19919777A1 (de) * | 1998-10-24 | 2000-07-13 | Sms Demag Ag | Verfahren zum Herstellen von Breitseitenplatten für Durchlaufkokillen |
Family Cites Families (25)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5150819A (ja) * | 1974-10-31 | 1976-05-04 | Kawasaki Steel Co | Renzokuchuzoyoigata |
| SU537749A1 (ru) * | 1975-07-01 | 1976-12-05 | Украинский научно-исследовательский институт металлов | Кристаллизатор |
| JPS54141330A (en) * | 1978-04-27 | 1979-11-02 | Nippon Kokan Kk | Surface curving process for cast mold for continuous cating |
| US4250950A (en) * | 1978-11-03 | 1981-02-17 | Swiss Aluminium Ltd. | Mould with roughened surface for casting metals |
| EP0158898B1 (de) * | 1984-04-13 | 1990-06-06 | Hans Horst | Stranggiessvorrichtung und Verfahren zu deren Herstellung |
| JPS6192756A (ja) * | 1984-10-12 | 1986-05-10 | Sumitomo Metal Ind Ltd | 鋳片表面割れ防止連続鋳造法および鋳型 |
| JPH0220645A (ja) * | 1988-07-08 | 1990-01-24 | Nkk Corp | 鋼の連続鋳造用鋳型 |
| JPH03128149A (ja) * | 1989-10-13 | 1991-05-31 | Ishikawajima Harima Heavy Ind Co Ltd | 双ロール式連鋳機 |
| FR2684904B1 (fr) * | 1991-12-11 | 1994-03-18 | Usinor Sacilor | Cylindre pour une machine de coulee continue de bandes metalliques, machine de coulee continue correspondante et procede de realisation d'un tel cylindre. |
| JP2974521B2 (ja) * | 1992-10-27 | 1999-11-10 | 新日本製鐵株式会社 | 薄肉鋳片の連続鋳造用鋳型及びその表面加工方法 |
| JPH07178526A (ja) * | 1993-11-09 | 1995-07-18 | Sumitomo Metal Ind Ltd | 連続鋳造方法および装置 |
| JP2971747B2 (ja) * | 1994-08-09 | 1999-11-08 | 住友重機械工業株式会社 | 連続鋳造用モールドのモールド壁 |
| US6024162A (en) * | 1994-12-28 | 2000-02-15 | Nippon Steel Corporation | Continuous casting method for billet |
| JPH08206786A (ja) * | 1995-01-31 | 1996-08-13 | Shinko Metal Prod Kk | 連続鋳造用鋳型 |
| DE19508169C5 (de) * | 1995-03-08 | 2009-11-12 | Kme Germany Ag & Co. Kg | Kokille zum Stranggießen von Metallen |
| JPH0994634A (ja) * | 1995-09-29 | 1997-04-08 | Kawasaki Steel Corp | 連続鋳造用水冷鋳型 |
| JPH09276994A (ja) * | 1996-04-22 | 1997-10-28 | Nippon Steel Corp | 連続鋳造用鋳型 |
| JP3380413B2 (ja) * | 1997-01-07 | 2003-02-24 | 新日本製鐵株式会社 | 溶鋼の連続鋳造用鋳型 |
| DE19748305A1 (de) * | 1997-10-31 | 1999-05-06 | Schloemann Siemag Ag | Stranggießkokille |
| DE19953905A1 (de) * | 1999-11-10 | 2001-05-17 | Sms Demag Ag | Verfahren und Vorrichtung zur Verminderung der Wärmeabfuhr einer Stranggußkokille |
| AU3011401A (en) * | 1999-12-29 | 2001-07-16 | Concast Standard A.G. | Method and device for working cavity walls in continuous casting moulds |
| EP1602424B2 (de) * | 2000-05-12 | 2013-03-27 | Nippon Steel & Sumitomo Metal Corporation | Gekühlte giesswalze zum kontinuierlichen stranggiessen von dünnen produkten und stranggiessverfahren |
| CN1201885C (zh) * | 2002-06-18 | 2005-05-18 | 鞍山科技大学 | 连铸镀层沟槽内壁结晶器 |
| DE10256751B4 (de) * | 2002-10-17 | 2019-09-12 | Sms Group Gmbh | Stranggießkokille zum Gießen von Strängen aus Metallen, insbesondere aus Stahlwerkstoffen |
| US7848950B2 (en) * | 2004-12-28 | 2010-12-07 | American Express Travel Related Services Company, Inc. | Method and apparatus for collaborative filtering of card member transactions |
-
2006
- 2006-03-09 WO PCT/EP2006/002164 patent/WO2006094803A1/de not_active Ceased
- 2006-03-09 CN CN2006800078160A patent/CN101137453B/zh not_active Expired - Lifetime
- 2006-03-09 ES ES06723315T patent/ES2864578T3/es not_active Expired - Lifetime
- 2006-03-09 EP EP06723315.5A patent/EP1855824B1/de not_active Expired - Lifetime
- 2006-03-09 JP JP2008500123A patent/JP4559520B2/ja not_active Expired - Lifetime
- 2006-03-09 CA CA2597100A patent/CA2597100C/en not_active Expired - Fee Related
- 2006-03-09 KR KR1020077016946A patent/KR101152678B1/ko not_active Expired - Lifetime
- 2006-03-10 US US11/885,808 patent/US20080173422A1/en not_active Abandoned
-
2011
- 2011-02-11 US US13/025,903 patent/US20110180231A1/en not_active Abandoned
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19919777A1 (de) * | 1998-10-24 | 2000-07-13 | Sms Demag Ag | Verfahren zum Herstellen von Breitseitenplatten für Durchlaufkokillen |
Also Published As
| Publication number | Publication date |
|---|---|
| CA2597100C (en) | 2013-01-22 |
| EP1855824A1 (de) | 2007-11-21 |
| ES2864578T3 (es) | 2021-10-14 |
| WO2006094803A1 (de) | 2006-09-14 |
| US20110180231A1 (en) | 2011-07-28 |
| CA2597100A1 (en) | 2006-09-14 |
| JP2008532767A (ja) | 2008-08-21 |
| CN101137453A (zh) | 2008-03-05 |
| KR101152678B1 (ko) | 2012-06-15 |
| KR20070110271A (ko) | 2007-11-16 |
| CN101137453B (zh) | 2012-09-05 |
| JP4559520B2 (ja) | 2010-10-06 |
| US20080173422A1 (en) | 2008-07-24 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2907511A1 (de) | Kuehlplatte fuer schachtoefen und verfahren zur herstellung derselben | |
| DE10243359A1 (de) | Strangpressform zum Wabenstrangpressen und Herstellungsverfahren dafür | |
| DE102007003548B3 (de) | Gießwalze für eine Zweiwalzengießvorrichtung und Zweiwalzengießvorrichtung | |
| EP1099496B1 (de) | Vorrichtung zur Verminderung der Wärmeabfuhr einer Stranggusskokille | |
| EP1499462A1 (de) | Anpassung des wärmeüberganges bei stranggiesskokillen, insbesondere im giessspiegelbereich | |
| DE4224078A1 (de) | Gittergießform zum Gießen von Akkumulatoren-Bleigittern und Verfahren zu deren Herstellung | |
| DE60000858T2 (de) | Verfahren und vorrichtung zum stranggiessen mit hoher geschwindigkeit | |
| DE102019213531B4 (de) | Werkzeugteil für ein Blechumformwerkzeug mit additiv erzeugtem Wirkflächenbereich und Verfahren zur Herstellung | |
| DE69530653T2 (de) | Strangpressdüse für Wabenstruktur | |
| EP1792675B1 (de) | Kokille zum Stranggiessen von Metall | |
| EP2483017B1 (de) | Giessform | |
| DE102005023745B4 (de) | Verfahren zum Herstellen einer Stranggiesskokille und Stranggiesskokille | |
| EP3083103B1 (de) | Giesskokille zum vergiessen von stahlschmelze | |
| EP3406368A1 (de) | Kokille zum stranggiessen von metallischen produkten | |
| WO2006094803A1 (de) | Verfahren zum herstellen einer stranggiesskokille und stranggiesskokille | |
| EP1019208B1 (de) | Kokillenrohr für eine stranggiesskokille zum stranggiessen von stählen, insbesondere peritektischen stählen | |
| DE69929382T2 (de) | Kühltrommel für eine Doppelrollen-Stranggussanlage | |
| EP1666797A1 (de) | Hitzeschildelement, Verfahren zu dessen Herstellung, Heisgasauskleidung und Brennkammer | |
| WO2011006635A1 (de) | Verbundbremsklotzsohle und verbundbremsklotz | |
| DE102005004486A1 (de) | Laufbuchse zum Eingießen in einen Motorblock | |
| WO2007071542A1 (de) | Beschichtung für eine kokille für eine stranggiessanlage und verfahren zur beschichtung | |
| EP0030308A1 (de) | Stranggiesskokille zum Giessen von Stahl | |
| DE19781990B4 (de) | Verbesserte Kokillenwandfläche für den Strangguss und Fertigungsverfahren | |
| DE10256751A1 (de) | Stranggiesskokille zum Giessen von Strängen aus Metallen, insbesondere aus Stahlwerkstoffen | |
| EP1520643B1 (de) | Verfahren zum Beschichten eines in einer Stranggiessanlage eingesetzten Kokillenkörpers |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20070615 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SMS SIEMAG AG |
|
| 17Q | First examination report despatched |
Effective date: 20110926 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SMS GROUP GMBH |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20200907 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 502006016457 Country of ref document: DE Owner name: SMS GROUP GMBH, DE Free format text: FORMER OWNER: SMS DEMAG AG, 40237 DUESSELDORF, DE |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502006016457 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1360819 Country of ref document: AT Kind code of ref document: T Effective date: 20210315 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20210217 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210518 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210617 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210517 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210617 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2864578 Country of ref document: ES Kind code of ref document: T3 Effective date: 20211014 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502006016457 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20210331 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20211118 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210331 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210309 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210331 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210309 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210417 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210617 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20060309 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230707 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250319 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20250320 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250325 Year of fee payment: 20 Ref country code: GB Payment date: 20250321 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20250425 Year of fee payment: 20 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210217 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 502006016457 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20260326 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20260308 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20260310 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK07 Ref document number: 1360819 Country of ref document: AT Kind code of ref document: T Effective date: 20260309 |