EP1748088B1 - Verfahren zur Herstellung eines Halbzeugs oder Bauteils von Fahrwerk- oder Strukturanwendungen im Kraftfahrzeug - Google Patents
Verfahren zur Herstellung eines Halbzeugs oder Bauteils von Fahrwerk- oder Strukturanwendungen im Kraftfahrzeug Download PDFInfo
- Publication number
- EP1748088B1 EP1748088B1 EP05016538A EP05016538A EP1748088B1 EP 1748088 B1 EP1748088 B1 EP 1748088B1 EP 05016538 A EP05016538 A EP 05016538A EP 05016538 A EP05016538 A EP 05016538A EP 1748088 B1 EP1748088 B1 EP 1748088B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- strip
- hot
- casting
- cold
- semifinished product
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Revoked
Links
- 239000011265 semifinished product Substances 0.000 title claims abstract description 30
- 238000000034 method Methods 0.000 title claims description 11
- 229910000838 Al alloy Inorganic materials 0.000 claims abstract description 34
- 238000005266 casting Methods 0.000 claims abstract description 15
- 238000004519 manufacturing process Methods 0.000 claims abstract description 11
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims abstract description 9
- 229910052782 aluminium Inorganic materials 0.000 claims abstract description 9
- 238000000137 annealing Methods 0.000 claims abstract description 7
- 238000005097 cold rolling Methods 0.000 claims abstract description 7
- 229910052719 titanium Inorganic materials 0.000 claims abstract 2
- 238000009864 tensile test Methods 0.000 claims description 9
- 238000012545 processing Methods 0.000 claims description 3
- 239000004411 aluminium Substances 0.000 claims 1
- 239000011777 magnesium Substances 0.000 abstract description 9
- FYYHWMGAXLPEAU-UHFFFAOYSA-N Magnesium Chemical compound [Mg] FYYHWMGAXLPEAU-UHFFFAOYSA-N 0.000 abstract description 5
- 229910052749 magnesium Inorganic materials 0.000 abstract description 5
- 238000005098 hot rolling Methods 0.000 abstract description 2
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 abstract 2
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 abstract 1
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 abstract 1
- RTAQQCXQSZGOHL-UHFFFAOYSA-N Titanium Chemical compound [Ti] RTAQQCXQSZGOHL-UHFFFAOYSA-N 0.000 abstract 1
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 abstract 1
- 229910052804 chromium Inorganic materials 0.000 abstract 1
- 239000011651 chromium Substances 0.000 abstract 1
- 229910052802 copper Inorganic materials 0.000 abstract 1
- 239000010949 copper Substances 0.000 abstract 1
- 239000012535 impurity Substances 0.000 abstract 1
- 229910052742 iron Inorganic materials 0.000 abstract 1
- WPBNNNQJVZRUHP-UHFFFAOYSA-L manganese(2+);methyl n-[[2-(methoxycarbonylcarbamothioylamino)phenyl]carbamothioyl]carbamate;n-[2-(sulfidocarbothioylamino)ethyl]carbamodithioate Chemical compound [Mn+2].[S-]C(=S)NCCNC([S-])=S.COC(=O)NC(=S)NC1=CC=CC=C1NC(=S)NC(=O)OC WPBNNNQJVZRUHP-UHFFFAOYSA-L 0.000 abstract 1
- 229910052710 silicon Inorganic materials 0.000 abstract 1
- 239000010703 silicon Substances 0.000 abstract 1
- 239000010936 titanium Substances 0.000 abstract 1
- 239000011701 zinc Substances 0.000 abstract 1
- 229910052725 zinc Inorganic materials 0.000 abstract 1
- 229910045601 alloy Inorganic materials 0.000 description 16
- 239000000956 alloy Substances 0.000 description 16
- 238000005260 corrosion Methods 0.000 description 9
- 230000007797 corrosion Effects 0.000 description 9
- 230000000052 comparative effect Effects 0.000 description 8
- 238000007711 solidification Methods 0.000 description 4
- 230000008023 solidification Effects 0.000 description 4
- 239000011572 manganese Substances 0.000 description 3
- 238000005275 alloying Methods 0.000 description 2
- 239000000470 constituent Substances 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 238000005259 measurement Methods 0.000 description 2
- 229910052706 scandium Inorganic materials 0.000 description 2
- 229910052726 zirconium Inorganic materials 0.000 description 2
- PWHULOQIROXLJO-UHFFFAOYSA-N Manganese Chemical compound [Mn] PWHULOQIROXLJO-UHFFFAOYSA-N 0.000 description 1
- QCWXUUIWCKQGHC-UHFFFAOYSA-N Zirconium Chemical compound [Zr] QCWXUUIWCKQGHC-UHFFFAOYSA-N 0.000 description 1
- 238000011109 contamination Methods 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 230000007774 longterm Effects 0.000 description 1
- 229910052748 manganese Inorganic materials 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 239000000047 product Substances 0.000 description 1
- 238000004064 recycling Methods 0.000 description 1
- SIXSYDAISGFNSX-UHFFFAOYSA-N scandium atom Chemical compound [Sc] SIXSYDAISGFNSX-UHFFFAOYSA-N 0.000 description 1
- 230000035945 sensitivity Effects 0.000 description 1
- 239000000779 smoke Substances 0.000 description 1
- 239000000725 suspension Substances 0.000 description 1
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/06—Alloys based on aluminium with magnesium as the next major constituent
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/06—Alloys based on aluminium with magnesium as the next major constituent
- C22C21/08—Alloys based on aluminium with magnesium as the next major constituent with silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22F—CHANGING THE PHYSICAL STRUCTURE OF NON-FERROUS METALS AND NON-FERROUS ALLOYS
- C22F1/00—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working
- C22F1/04—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon
- C22F1/047—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon of alloys with magnesium as the next major constituent
Definitions
- the invention relates to a method for producing a semifinished product or component for chassis or structural applications in motor vehicles.
- components such as parts of the chassis or the body structure, made of aluminum materials are used increasingly for the production of motor vehicles.
- These are usually made of semi-finished products consisting of aluminum alloys based on an AlMgMn aluminum alloy with Mg contents of 2 to 3.5 wt .-%.
- This aluminum alloy ensures sufficiently high strength combined with good resistance to intergranular corrosion, especially in uncoated applications. Since in the manufacture of the chassis and / or structural components existing from said aluminum alloy semi-finished products are usually subjected to several forming steps, there is a desire to extend the forming limits of the semi-finished products, such as aluminum sheets, tubes or profiles.
- hot forming processes such as hot hydroforming, hydroforming with hot media, or deep drawing with heated tools, are increasingly being used in the forming operations.
- degree of deformation of the aluminum semi-finished products can be significantly increased when using hot forming processes.
- Hot forming processes significantly increase the degree of deformation of the aluminum semi-finished products. Due to the softening processes taking place during hot forming, however, the components or semi-finished products consisting of the AlMgMn aluminum alloys used today have a lower strength than the previously cold-worked components used.
- the object of the present invention is to provide a method for producing a semifinished product or component which, with good resistance to intergranular corrosion and recyclability, has sufficient strength even after hot forming.
- the aluminum alloy to be used according to the invention makes it possible to produce components which are not only resistant to intergranular corrosion but also have higher strength after hot working compared with the aluminum alloys used hitherto. Moreover, since the aluminum alloy to be used according to the invention contains only standard alloy components, it is very easy to recycle and can be introduced without problems into the scrap circuits of the automotive industry (Alt-Autover Aunt), as well as the semis manufacturer.
- a corresponding aluminum alloy leads to a further increase in the yield strength Rp0.2 at room temperature after hot deformation with constant resistance to intergranular corrosion, while the elongation at break values remain the same.
- semifinished products or components produced from the aluminum alloy to be used according to the invention can be used particularly well for suspension and structural applications in motor vehicles, since they have an improved yield strength at room temperature, in particular after hot working, with constant corrosion resistance .
- a component differs from the semifinished product in that the component has been subjected to further process steps in order to be used, for example, directly in the body of the motor vehicle.
- the semifinished product thus represents the starting product for the components .
- the suitability of the semi-finished product or component for structural applications in the motor vehicle can be further improved by subjecting the semifinished product to hot forming with a degree of deformation of at least 15% and at most 50% to 120% at a temperature of 200 to 350
- the semifinished product has an elongation at break A 5 of at least 50% in the hot tensile test and the semifinished product has a yield strength at room temperature Rp0.2 of at least 150 MPa.
- the elongation at break values A 5 in the hot tensile test were measured at the respective hot forming temperatures with a corresponding proportional rod.
- the yield strength Rp0.2 of the structural parts clearly exceeds the yield strength Rp0.2 from the known AlMgMn aluminum alloy with an Mg content of 2 to 3.5% by weight of produced structural parts after hot working , without showing any sensitivity to intergranular corrosion.
- a semifinished product or component which is further improved with regard to the yield strength at room temperature and the elongation at break can be made available by virtue of the semifinished product being subjected to hot forming with a degree of deformation of at least 15% and a maximum of 60%.
- 90% at a temperature of 250 to 350 ° C has been subjected while having an elongation at break A 5 of at least 60% in the hot tensile test and that the semi-finished product after hot working has a yield strength at room temperature of at least 165 Mpa.
- the hot tensile tests were carried out on proportional bars at the hot-forming temperatures mentioned.
- the area-related mass loss according to ASTM G 67 after a heat treatment of 17 hours at 130 ° C is a maximum of 5 mg / cm 2 .
- the semi-finished products according to the invention therefore have a particularly good resistance to intergranular corrosion and are particularly suitable for use as or for the production of chassis or structural parts in motor vehicles.
- the inventive method for producing a semifinished product or component for a chassis or structural applications smoke be provided by casting a cast strip or a casting strip of an aluminum alloy to be used according to the invention, the cast bar or optionally the casting strip is hot rolled, the hot rolled cast ingot or Cold rolled strip and the cold rolled strip is a final annealing, wherein the strip has a thickness of at least 1 mm and a hot working with a degree of deformation of at least 15% and a maximum of 50% to 120% at a temperature of 200 to 350 ° C is subjected and the semifinished product has an elongation at break A 5 of at least 50% in the hot tensile test and the semifinished product after hot forming has a yield strength Rp0.2 at room temperature of at least 150 MPa. Due to the properties of the aluminum alloy to be used according to the invention, it is ensured in the described production method that sheets produced from the strip, despite used hot forming processes, have an improved yield strength at room temperature with constant elongation at break values.
- Solidification introduced into the strip by hot rolling can be reduced by subjecting the strip to annealing prior to cold rolling.
- the cold rolled strip in this case has only the solidifications introduced by cold rolling into the strip.
- the solidifications introduced into the strip by the cold rolling are reduced again by at least one intermediate annealing during cold rolling. All of the aforementioned measures serve to increase the formability in the production of aluminum strip for semi-finished products, without the structural parts produced have too low a yield point.
- Fig. 1 the elongation at break values of three different aluminum alloys are shown as a function of the temperature.
- the elongation at break A 5 was measured according to the DIN standard DIN EN 10 002 with corresponding proportional bars, wherein a strain rate of 0.1 s -1 has been set.
- the temperature was varied during the elongation at break measurements between 30 ° C and 450 ° C.
- the comparative aluminum alloys A and B were compared with the aluminum alloy C to be used in the present invention.
- the conventional aluminum alloy A is an AlMg4.5Mn0.7 alloy having a relatively high magnesium content of 4.5% by weight and the comparative alloy B is an AlMg3.5Mn alloy having a magnesium content of 2 to 3.5% by weight.
- the aluminum alloy to be used according to the invention has the following proportions of alloy constituents in% by weight: 0 . 1 % ⁇ S ⁇ i ⁇ 0 . 2 % . 0 . 2 % ⁇ F ⁇ e ⁇ 0 . 35 % . C ⁇ u ⁇ 0 . 05 % . 0 . 6 % ⁇ M ⁇ n ⁇ 1 . 1 % . 3 . 1 % ⁇ M ⁇ G ⁇ 1 . 1 % . C ⁇ r ⁇ 0 . 3 % . Z ⁇ n ⁇ 0 . 4 % . T ⁇ i ⁇ 0 . 15 % . Rest aluminum.
- the aluminum alloy C to be used according to the invention in comparison to the conventional comparative alloys A and B has almost identical elongation at break values as a function of the temperature in the hot tensile test.
- the comparative alloy A shows as expected, due to the high magnesium content of 4.5 wt .-%, the largest values for the yield strength after hot working.
- the value of the yield strength for the comparative alloy A is about 175 MPa at a hot working temperature of 350 ° C.
- Comparative alloy B has only reached a value of 140 MPa for the yield strength Rp0.2 at room temperature at the same hot forming temperature.
- the embodiment of the aluminum alloy to be used according to the invention reaches values of significantly more than 150 MPa. Also in the other measured values, for example at 250 ° C., the values for the measured yield strength of the exemplary embodiment of the aluminum alloy to be used according to the invention are significantly above those of the comparative alloy B but below the values for the comparative alloy A.
- the comparison alloy A is more susceptible to intercrystalline corrosion due to the higher MG content, so that it is not advantageous, especially in long-term use in chassis or structural application in the motor vehicle.
- an aluminum alloy can be provided which, despite improved yield strength after hot working, has good intergranular corrosion resistance and good elongation at break properties during hot working.
Landscapes
- Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Organic Chemistry (AREA)
- Metallurgy (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Crystallography & Structural Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Metal Rolling (AREA)
- Treatments Of Macromolecular Shaped Articles (AREA)
- Polyesters Or Polycarbonates (AREA)
- Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
- Conductive Materials (AREA)
Description
- Die Erfindung betrifft ein Verfahren zur Herstellung eines Halbzeugs oder Bauteils für Fahrwerk-oder Strukturanwendungen im Kraftfahrzeuge.
- In der Automobilindustrie werden zur Herstellung von Kraftfahrzeugen zunehmend Bauteile, beispielsweise Teile des Fahrwerkes oder der Karosseriestruktur, aus Aluminiumwerkstoffen eingesetzt. Diese werden in der Regel aus Halbzeugen bestehend aus Aluminiumlegierungen basierend auf einer AlMgMn-Aluminiumlegierung mit Mg-Gehalten von 2 bis 3,5 Gew.-% hergestellt. Diese Aluminiumlegierung gewährleistet eine ausreichend hohe Festigkeit bei gleichzeitig guter Beständigkeit gegen interkristalline Korrosion, insbesondere im unbeschichteten Einsatz. Da bei der Herstellung der Fahrwerks- und/oder Strukturbauteile die aus der genannten Aluminiumlegierung bestehenden Halbzeuge zumeist mehreren Umformschritten unterzogen werden, besteht der Wunsch, die Formgebungsgrenzen der Halbzeuge, beispielsweise der Aluminiumbleche, -rohre oder -profile, zu erweitern. Deshalb werden bei den Umformungen vermehrt Warmumformprozesse, beispielsweise Warm-Innenhochdruckumformen, Hydroformen mit heißen Medien oder ein Tiefziehen mit beheizten Werkzeugen verwendet. Zwar lassen sich bei der Verwendung von Warmumformprozessen die Umformgrade der Aluminiumhalbzeuge deutlich steigern. Aufgrund der beim Warmumformprozessen die Umformgrade der Aluminiumhalbzeuge deutlich steigern. Aufgrund der beim Warmumformen stattfindenden Entfestigungsvorgänge weisen die aus den heute eingesetzten AlMgMn-Aluminiumlegierungen bestehenden Bauteile oder Halbzeuge jedoch eine geringere Festigkeit auf, als die bisher eingesetzten, kaltverformten Bauteile.
- Um die Festigkeit von warmumgeformten Bauteilen zu vergrößern ist es bekannt, Scandium und Zirconium als Legierungsbestandteile der AlMgMn-Legierung zuzusetzen. Problematisch sind diese Legierungen jedoch einerseits hinsichtlich des Recyclings, da die Legierungselemente Sc und Zr in den üblichen Standard-Aluminiumlegierungen nicht enthalten sind und daher mit diesen nicht eingeschmolzen werden sollten. Andererseits führen diese Elemente in der Regel zu Verarbeitungsproblemen bei Aluminiumlegierungen. Halbzeuge bestehend aus einer ähnlichen Aluminiumlegierung sind beispielsweise aus der
japanischen Patentanmeldung JP 05-247576 A - Hiervon ausgehend liegt der vorliegenden Erfindung damit die Aufgabe zugrunde, ein Verfahren zur Herstellung eines Halbzeugs oder Bauteils zur Verfügung zu stellen, welches bei guter Beständigkeit gegen interkristalline Korrosion und Recyclingfähigkeit auch nach einem Warmumformen eine ausreichende Festigkeit aufweist.
- Die Aufgabe wird durch ein Verfahren mit den Merkmalen des Patentanspruchs 1 gelöst.
- Gemäß der Erfindung wird eine Aluminiumlegierung zur Herstellung von Bauteilen für Fahrzeuge, insbesondere Kraftfahrzeuge verwendet, die folgende Legierungsbestandteile in Gew. -% aufweist:
- 0,1 % ≤ 0,2 %,
- 0,2 % ≤ 0,35 %,
- Cu ≤ 0,005 %,
- 0,6 % ≤ Mn ≤ 1,1 %,
- 3,1 % ≤ Mg ≤ 3,9 %,
- Cr ≤ 0,3 %,
- Zn ≤ 0,4 %,
- Ti ≤ 0,15 %,
- Verunreinigung einzeln ≤ 0,05 %, in Summe max. 0,15 %, Rest A1.
- Aufgrund der Kombination des Magnesium-Gehaltes mit dem ausgewählten Mangan-Gehalt ermöglicht die erfindungsgemäß zu verwendende Aluminiumlegierung die Herstellung von Bauteilen, welche nicht nur gegenüber interkristalliner Korrosion beständig sind, sondern auch nach einem Warmumformen im Vergleich zu den bisher eingesetzten Aluminiumlegierungen eine höhere Festigkeit aufweisen. Da die erfindungsgemäß zu verwendende Aluminiumlegierung darüber hinaus nur Standard-Legierungskomponenten enthält, ist diese sehr gut rezyklierbar und kann ohne Probleme in die Schrottkreisläufe der Automobilindustrie (Alt-Autoverordnung), aber auch der Halbzeughersteller eingeführt werden.
- Eine entsprechende Aluminiumlegierung führt bei gleich bleibenden Bruchdehnungswerten zu einer weiteren Steigerung der Dehngrenze Rp0,2 bei Raumtemperatur nach einer Warmumformung bei gleich bleibender Beständigkeit gegen interkristalline Korrosion.
- Wie bereits ausgeführt, können Halbzeuge oder Bauteile hergestellt aus der erfindungsgemäß zu verwendenden Aluminiumlegierung besonders gut für Fahrwerks- und Strukturanwendungen im Kraftfahrzeug eingesetzt werden, da diese bei gleich bleibender Korrosionsbeständigkeit eine verbesserte Dehngrenze bei Raumtemperatur, insbesondere nach einer Warmumformung, aufweisen. Ein Bauteil unterscheidet sich dabei vom Halbzeug dadurch, dass das Bauteil weiteren Verfahrenschritten unterzogen worden ist, um beispielsweise unmittelbar in der Karosserie des Kraftfahrzeugs eingesetzt zu werden. Das Halbzeug stellt also das Ausgangsprodukt für die Bauteile dar.
- In Verbindung mit der erfindungsgemäß zu verwendenden Aluminiumlegierung kann die Eignung des Halbzeugs oder Bauteils für Strukturanwendungen im Kraftfahrzeug dadurch weiter verbessert werden, dass das Halbzeug einer Warmumformung mit einem Umformgrad von mindestens 15 % und maximal 50 % bis 120 % bei einer Temperatur von 200 bis 350 °C unterzogen worden ist, das Halbzeug dabei eine Bruchdehnung A5 von mindestens 50 % im Warmzugversuch aufweist und dass das Halbzeug eine Dehngrenze bei Raumtemperatur Rp0,2 von mindestens 150 MPa aufweist. Die Bruchdehnungswerte A5 im Warmzugversuch wurden bei den jeweiligen Warmumformtemperaturen mit einem entsprechenden Proportionalstab gemessen. Die Dehngrenze Rp0,2 der Strukturteile übersteigt nach der Warmumformung die Dehngrenze Rp0,2 aus der bekannten AlMgMn-Aluminiumlegierung mit einem Mg -Gehalt von 2 - 3.5 Gew.-% hergestellter Strukturteile deutlich, ohne eine Empfindlichkeit gegen interkristalline Korrosion zu zeigen.
- Ein hinsichtlich der Dehngrenze bei Raumtemperatur und der Bruchdehnung weiter verbessertes Halbzeug oder Bauteil kann, dadurch zur Verfügung gestellt werden, dass das Halbzeug einer Warmumformung mit einem Umformgrad von mindestens 15 % und maximal 60 % bis 90 % bei einer Temperatur von 250 bis 350 °C unterzogen worden ist und dabei eine Bruchdehnung A5 von mindestens 60 % im Warmzugversuch aufweist und dass das Halbzeug nach der Warmumformung eine Dehngrenze bei Raumtemperatur von mindestens 165 Mpa aufweist. Auch hier wurden die Warmzugversuche an Proportionalstäben bei den genannten Warmumformtemperaturen durchgeführt.
- Gemäß einer nächsten vorteilhaften Ausführungsform beträgt der flächenbezogene Massenverlust nach ASTM G 67 nach einer thermischen Behandlung von 17 Stunden bei 130 °C maximal 5 mg/cm2. Die erfindungsgemäß hergestellten Halbzeuge weisen daher eine besonders gute Beständigkeit gegen interkristalline Korrosion auf und eignen sich insbesondere für den Einsatz als bzw. zur Herstellung von Fahrwerks- oder Strukturteilen im Kraftfahrzeug.
- Das erfindungsgemäße Verfahren zur Herstellung eines Halbzeugs oder Bauteils für ein Fahrwerk- oder Strukturanwendungen rauch dadurch bereit gestellt werden, dass ein Gießbarren oder ein Gießband aus einer erfindungsgemäß zu verwendenden Aluminiumlegierung gegossen wird, der Gießbarren oder optional das Gießband warmgewalzt wird, der warmgewalzte Gießbarren oder das Gießband kaltgewalzt werden und das kaltgewalzte Band einer Endglühung zugeführt wird, wobei das Band eine Dicke von mindestens 1 mm aufweist und einer Warmumformung mit einem Umformgrad von mindestens 15 % und maximal 50 % bis 120 % bei einer Temperatur von 200 bis 350 °C unterzogen wird und das Halbzeug dabei eine Bruchdehnung A5 von mindestens 50 % im Warmzugversuch aufweist und das Halbzeug nach der Warmumformung eine Dehngrenze Rp0,2 bei Raumtemperatur von mindestens 150 MPa aufweist. Durch die Eigenschaften der erfindungsgemäß zu verwendenden Aluminiumlegierung wird bei dem beschriebenen Herstellverfahren gewährleistet, dass aus dem Band hergestellte Bleche trotz verwendeter Warmumformprozesse eine verbesserte Dehngrenze bei Raumtemperatur bei gleich bleibenden Bruchdehnungswerten aufweisen.
- Wird der Gießbarren oder das Gießband nach dem Gießen und vor den weiteren Verarbeitungsschritten homogenisiert, kann ein Aluminiumband mit verbesserter Umformbarkeit hergestellt werden.
- Verfestigungen, welche in das Band durch das Warmwalzen eingebracht worden sind, können dadurch verringert werden, dass das Band vor dem Kaltwalzen einer Glühung unterzogen wird. Das kaltgewalzte Band weist in diesem Fall nur die vom Kaltwalzen in das Band eingebrachten Verfestigungen auf.
- Vorzugsweise werden die durch das Kaltwalzen in das Band eingebrachten Verfestigungen dadurch wieder abgebaut, dass während des Kaltwalzens mindestens eine Zwischenglühung erfolgt. Alle zuvor genannten Maßnahmen dienen dazu, bei der Herstellung des Aluminiumbandes für Halbzeuge die Umformbarkeit zu steigern, ohne dass die hergestellten Strukturteile eine zu geringe Dehngrenze aufweisen.
- Es gibt nun eine Vielzahl von Möglichkeiten das erfindungsgemäße Verfahren zur Herstellung eines Halbzeugs oder Bauteils auszugestalten oder weiterzubilden. Hierzu wird verwiesen einerseits die dem Patentanspruch 1, nachgeordneten Patentansprüchen sowie der Beschreibung eines Ausführungsbeispiels in Verbindung mit der Zeichnung. Die Zeichnung zeigt
- Fig. 1
- in einem Diagramm die Bruchdehnung eines Ausführungsbeispiels der erfindungsgemäß zu verwenden Aluminiumlegierung im Vergleich mit anderen herkömmlichen Aluminiumlegierungen in Abhängigkeit von der Umformtemperatur im Warmzugversuch und
- Fig. 2
- in einem Diagramm die Dehngrenze Rp0,2 gemessen bei Raumtemperatur des Ausführungsbeispiels aus
Fig. 1 im Vergleich zu konventionellen Aluminiumlegierungen in Abhängigkeit von der Temperatur bei einer Warmumformung. - In der
Fig. 1 sind die Bruchdehnungswerte von drei verschiedenen Aluminiumlegierungen in Abhängigkeit von der Temperatur dargestellt. Die Bruchdehnung A5 wurde nach der DIN-Norm DIN EN 10 002 mit entsprechenden Proportionalstäben gemessen, wobei eine Dehnrate von 0,1 s-1 eingestellt worden ist. Die Temperatur wurde bei den Bruchdehnungsmessungen zwischen 30°C und 450°C variiert. Die Vergleichs-Aluminiumlegierungen A und B wurden mit der erfindungsgemäß zu verwendenden Aluminiumlegierung C verglichen. Bei der konventionellen Aluminiumlegierung A handelt es sich um eine AlMg4,5Mn0,7-Legierung mit einem relativ hohen Magnesiumanteil von 4,5 Gew.-% und bei der Vergleichslegierung B um eine AlMg3,5Mn-Legierung mit einem Magnesium-Gehalt von 2 bis 3,5 Gew.-%. Die erfindungsgemäß zu verwendende Aluminiumlegierung weist die folgenden Anteile an Legierungsbestandteilen in Gew.-% auf:
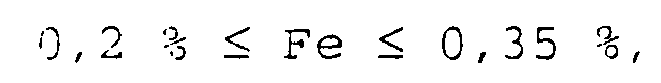


Rest Aluminium. - Wie aus
Fig. 1 zu erkennen ist, weist die erfindungsgemäß zu verwendende Aluminiumlegierung C im Vergleich zu den konventionellen Vergleichslegierungen A und B nahezu identische Bruchdehnungswerte in Abhängigkeit von der Temperatur im Warmzugversuch auf. - Unterschiede zwischen den drei Legierungen ergeben sich aber im Vergleich der Dehngrenze Rp0,2 bei Raumtemperatur gemessen nach einer Umformung mit einem Umformgrad von 15 % in Abhängigkeit von der Umformtemperatur. So zeigt die Vergleichslegierung A erwartungsgemäß aufgrund des hohen Magnesium-Gehalts von 4,5 Gew.-% die größten Werte für die Dehngrenze nach einer Warmumformung. Der Wert der Dehngrenze für die Vergleichslegierung A beträgt bei einer Warmumformtemperatur von 350 °C etwa 175 MPa. Die Vergleichslegierung B hat bei gleicher Warmumformtemperatur lediglich einen Wert von 140 MPa für die Dehngrenze Rp0,2 bei Raumtemperatur erreicht. Das Ausführungsbeispiel der erfindungsgemäß zu verwendenden Aluminiumlegierung dagegen erreicht Werte von deutlich über 150 MPa. Auch in den übrigen Messwerten, beispielsweise bei 250 °C, liegend die Werte für die gemessene Dehngrenze des Ausführungsbeispiels der erfindungsgemäß zu verwendenden Aluminiumlegierung deutlich über denen der Vergleichslegierung B jedoch unterhalb der Werte für die Vergleichslegierung A.
- Allerdings ist die Vergleichslegierung A aufgrund des höheren MG-Gehaltes anfälliger hinsichtlich interkristalliner Korrosion, so dass diese, insbesondere im Langzeiteinsatz bei Fahrwerks- oder Strukturanwendung im Kraftfahrzeug nicht vorteilhaft ist.
- Wie aus den Diagrammen aus der
Fig. 1 und2 zu erkennen ist, kann mit der erfindungsgemäß zu verwendenden Aluminiumlegierung eine Aluminiumlegierung zur Verfügung gestellt werden, welche, trotz verbesserter Dehngrenze nach einer Warmumformung, eine gute Beständigkeit gegen interkristalline Korrosion und gute Bruchdehnungseigenschaften während einer Warmumformung aufweist. - Ferner wurden noch die in der untenstehenden Tabelle angegebenen Messwerte für die Bruchdehnung A5 im Warmzugversuch und der Dehngrenze Rp0,2 gemessen bei Raumtemperatur nach dem Warmumformungen an Proben bestehend aus der erfindungsgemäß zu verwendenden Aluminiumlegierung C ermittelt. Auch diese Messungen wurden gemäß DIN EN 10 002 durchgeführt. Die Warmumformungen wurden dabei mit einem Umformgrad von 15 % durchgeführt.
Warmumformtemperatur [°C] Bruchdehnung A5 [%] Dehngrenze Rp0,2 bei Raumtemperatur [MPa] 330 100 160 300 90 168 275 80 175 230 60 190 - Deutlich ist das Ansteigen der Dehngrenze Rp0,2 und das Absinken der Bruchdehnungswerte mit abnehmender Warmumformtemperatur zu erkennen. Dies überrascht insofern nicht, da mit abnehmender Temperatur bei der Warmumformung vermehrt Verfestigungen in die Probenkörper eingebracht werden, die nicht mehr abgebaut werden und zu einer Steigerung der Dehngrenze Rp0,2 führen. Bei höheren Warmumformtemperaturen werden diese wieder abgebaut, wobei die Dehngrenze Rp0,2 auch nach einer Warmumformung bei 330 °C noch 160 MPa beträgt.
Claims (4)
- Verfahren zur Herstellung eines Halbzeugs oder Bauteils von Fahrwerk- oder Strukturanwendungen im Kraftfahrzeug,
dadurch gekennzeichnet, dass
ein Gießbarren oder -band unter Verwendung einer Aluminiumlegierung, aufweisend die folgenden Anteile in Gew.-%:
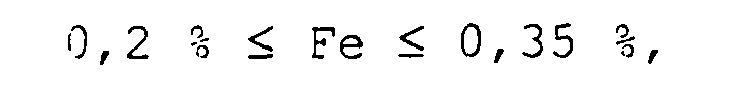
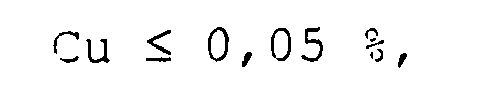


Rest Aluminium, unvermeidbare Begleitelemente einzeln ≤ 0,05 %, in Summe max. 0,15 %.
gegossen wird, der Gießbarren oder optional das Gießband zu einem Warmband warmgewalzt wird, das Warmband oder das Gießband kaltgewalzt wird und das kaltgewalzte Band einer Endglühung zugeführt wird, wobei das Band eine Dicke von mindestens 1 mm aufweist und einer Warmumformung mit einem Umformgrad von mindestens 15 % und maximal 50 % bis 120 % bei einer Temperatur von 200 bis 350 °C unterzogen wird und das Halbzeug dabei eine Bruchdehnung A5 von mindestens 50 % im Warmzugversuch aufweist und das Halbzeug nach der Warmumformung eine Dehngrenze Rp0,2 bei Raumtemperatur von mindestens 150 MPa aufweist. - Verfahren nach Anspruch 1,
dadurch gekennzeichnet, dass
der Gießbarren oder das Gießband nach dem Gießen und vor den weiteren Verarbeitungsschritten homogenisiert wird. - Verfahren nach Anspruch 1 oder 2,
dadurch gekennzeichnet, dass
das Warmband oder Gießband vor dem Kaltwalzen einer Glühung unterzogen wird. - Verfahren nach Anspruch 1 bis 3,
dadurch gekennzeichnet, dass
während des Kaltwalzens mindestens eine Zwischenglühung erfolgt.
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP05016538A EP1748088B1 (de) | 2005-07-29 | 2005-07-29 | Verfahren zur Herstellung eines Halbzeugs oder Bauteils von Fahrwerk- oder Strukturanwendungen im Kraftfahrzeug |
| PL05016538T PL1748088T3 (pl) | 2005-07-29 | 2005-07-29 | Sposób wytwarzania półwyrobu lub elementu konstrukcyjnego do zastosowań w podwoziu lub strukturze pojazdu mechanicznego |
| ES05016538T ES2380343T3 (es) | 2005-07-29 | 2005-07-29 | Procedimiento para la producción de un producto semiacabado o una pieza de construcción en aplicaciones de chasis o de mecanismos estructurales en vehículo motorizado |
| PT05016538T PT1748088E (pt) | 2005-07-29 | 2005-07-29 | Método para a produção de um produto semi-acabado ou uma peça de construção de aplicações em mecanismo de translação ou estruturais em veículo motorizado |
| AT05016538T ATE540132T1 (de) | 2005-07-29 | 2005-07-29 | Verfahren zur herstellung eines halbzeugs oder bauteils von fahrwerk- oder strukturanwendungen im kraftfahrzeug |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP05016538A EP1748088B1 (de) | 2005-07-29 | 2005-07-29 | Verfahren zur Herstellung eines Halbzeugs oder Bauteils von Fahrwerk- oder Strukturanwendungen im Kraftfahrzeug |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1748088A1 EP1748088A1 (de) | 2007-01-31 |
| EP1748088B1 true EP1748088B1 (de) | 2012-01-04 |
Family
ID=34982200
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05016538A Revoked EP1748088B1 (de) | 2005-07-29 | 2005-07-29 | Verfahren zur Herstellung eines Halbzeugs oder Bauteils von Fahrwerk- oder Strukturanwendungen im Kraftfahrzeug |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP1748088B1 (de) |
| AT (1) | ATE540132T1 (de) |
| ES (1) | ES2380343T3 (de) |
| PL (1) | PL1748088T3 (de) |
| PT (1) | PT1748088E (de) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2415895B2 (de) * | 2010-08-02 | 2019-07-31 | Benteler Automobiltechnik GmbH | Verfahren zur Herstellung eines Blechformteils für Kraftfahrzeuge |
| KR102078945B1 (ko) * | 2015-06-05 | 2020-02-19 | 노벨리스 인크. | 고 강도 5xxx 알루미늄 합금들 및 이를 만드는 방법들 |
| CN105543741A (zh) * | 2015-12-17 | 2016-05-04 | 西南铝业(集团)有限责任公司 | 一种铝合金的中间退火工艺及汽车覆盖件用铝合金 |
| CN105463270A (zh) * | 2016-01-06 | 2016-04-06 | 熊超 | 一种可氧化着色的压铸铝合金 |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2579865B2 (ja) * | 1992-05-01 | 1997-02-12 | 株式会社神戸製鋼所 | 負圧缶ステイオンタブ式エンド用Al合金板及びその製造方法 |
| JP3523687B2 (ja) * | 1994-05-30 | 2004-04-26 | 住友軽金属工業株式会社 | 曲げ加工性に優れたステイオンタブ用アルミニウム合金板材およびその製造方法 |
| JP3270710B2 (ja) * | 1996-04-10 | 2002-04-02 | 東洋鋼鈑株式会社 | 絞りしごき缶用樹脂被覆アルミニウム合金板の製造方法 |
| JP3270709B2 (ja) * | 1996-04-10 | 2002-04-02 | 東洋鋼鈑株式会社 | 絞りしごき缶用樹脂被覆アルミニウム合金板の製造方法 |
| JP3270684B2 (ja) * | 1996-04-18 | 2002-04-02 | 東洋鋼鈑株式会社 | 絞りしごき缶用樹脂被覆アルミニウム合金板 |
| JP2000008133A (ja) * | 1998-06-23 | 2000-01-11 | Furukawa Electric Co Ltd:The | 耐落下強度に優れる缶蓋用アルミニウム合金板およびその製造方法 |
| JP2000144297A (ja) * | 1998-11-06 | 2000-05-26 | Furukawa Electric Co Ltd:The | 低温での靭性に優れるアルミニウム合金溶接継手とこれを使用した構造材料 |
| US7713470B2 (en) * | 2002-05-30 | 2010-05-11 | Honda Giken Kogyo Kabushiki Kaisha | Die casting having high toughness |
| FR2851579B1 (fr) * | 2003-02-26 | 2005-04-01 | Pechiney Rhenalu | PROCEDE D'EMBOUTISSAGE A TIEDE DE PIECES EN ALLIAGE A1-Mg |
-
2005
- 2005-07-29 EP EP05016538A patent/EP1748088B1/de not_active Revoked
- 2005-07-29 ES ES05016538T patent/ES2380343T3/es not_active Expired - Lifetime
- 2005-07-29 PL PL05016538T patent/PL1748088T3/pl unknown
- 2005-07-29 PT PT05016538T patent/PT1748088E/pt unknown
- 2005-07-29 AT AT05016538T patent/ATE540132T1/de active
Also Published As
| Publication number | Publication date |
|---|---|
| ES2380343T3 (es) | 2012-05-10 |
| PT1748088E (pt) | 2012-04-12 |
| EP1748088A1 (de) | 2007-01-31 |
| PL1748088T3 (pl) | 2012-05-31 |
| ATE540132T1 (de) | 2012-01-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3314031B1 (de) | Hochfestes und gut umformbares almg-band sowie verfahren zu seiner herstellung | |
| EP2770071B1 (de) | Aluminiumlegierung zur Herstellung von Halbzeugen oder Bauteilen für Kraftfahrzeuge, Verfahren zur Herstellung eines Aluminiumlegierungsbands aus dieser Aluminiumlegierung sowie Aluminiumlegierungsband und Verwendungen dafür | |
| EP1683882B1 (de) | Abschreckunempfindliche Aluminiumlegierung sowie Verfahren zum Herstellen eines Halbzeuges aus dieser Legierung | |
| EP2270249B1 (de) | AlMgSi-Band für Anwendungen mit hohen Umformungsanforderungen | |
| EP2570509B1 (de) | Herstellverfahren für AlMgSi-Aluminiumband | |
| DE112008003052T5 (de) | Produkt aus Al-Mg-Zn-Knetlegierung und Herstellungsverfahren dafür | |
| EP3176275B2 (de) | Aluminium-silizium-druckgusslegierung, verfahren zur herstellung eines druckgussbauteils aus der legierung und karosseriekomponente mit einem druckgussbauteil | |
| EP2067871B1 (de) | Aluminiumband für lithografische Druckplattenträger und dessen Herstellung | |
| EP2888382B2 (de) | Gegen interkristalline korrosion beständiges aluminiumlegierungsband und verfahren zu seiner herstellung | |
| EP3825428A1 (de) | Druckgussbauteil und verfahren zur herstellung eines druckgussbauteils | |
| WO2002083967A1 (de) | VERFAHREN ZUR HERSTELLUNG VON AlMn-BÄNDERN ODER -BLECHEN | |
| EP2192202B1 (de) | Aluminiumband für lithographische Druckplattenträger mit hoher Biegewechselbeständigkeit | |
| EP3077556B1 (de) | Verfahren zur bearbeitung einer dispersionsgehärteten platinzusammensetzung | |
| EP2703508B1 (de) | Gegen interkristalline Korrosion beständige Aluminiumlegierung | |
| DE102015007929A1 (de) | Aluminium-Gusslegierung, Verfahren zum Herstellen eines Bauteils aus einer Aluminium-Gusslegierung und Verwendung einer Aluminium-Gusslegierung | |
| EP3423606B1 (de) | Al-gusslegierung | |
| EP1748088A1 (de) | Warm- und kaltumformbare Aluminiumlegierung vom Typ Al-Mg-Mn | |
| EP1664357B1 (de) | verwendung eines stahls zur herstellung von ketten, verfahren zur herstellung einer kette und damit hergestellte kette | |
| EP2924135B1 (de) | Verfahren zur Herstellung eines Bandes aus einer hochumformbaren, mittelfesten Aluminiumlegierung für Halbzeuge oder Bauteile von Kraftfahrzeugen | |
| EP2426228B1 (de) | Magnesiumblechhalbzeuge mit verbessertem Kaltumformvermögen | |
| DE102010020268A1 (de) | Aluminium-Magnesium-Legierungsprodukt für geformte Autmobilteile |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK YU |
|
| 17P | Request for examination filed |
Effective date: 20070723 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20090403 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RTI1 | Title (correction) |
Free format text: PROCESS FOR PRODUCING A SEMI-FINISHED PRODUCT OR COMPONENT FOR CHASSIS OR STRUCTURAL AUTOMOTIVE APPLICATIONS |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: HYDRO ALUMINIUM DEUTSCHLAND GMBH |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 540132 Country of ref document: AT Kind code of ref document: T Effective date: 20120115 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502005012285 Country of ref document: DE Effective date: 20120308 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20120330 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2380343 Country of ref document: ES Kind code of ref document: T3 Effective date: 20120510 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20120104 |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E013501 Country of ref document: HU |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120404 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120504 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120405 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: NOVELIS, INC. Effective date: 20121004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R026 Ref document number: 502005012285 Country of ref document: DE Effective date: 20121004 |
|
| BERE | Be: lapsed |
Owner name: HYDRO ALUMINIUM DEUTSCHLAND G.M.B.H. Effective date: 20120731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120731 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| PLAF | Information modified related to communication of a notice of opposition and request to file observations + time limit |
Free format text: ORIGINAL CODE: EPIDOSCOBS2 |
|
| R26 | Opposition filed (corrected) |
Opponent name: NOVELIS, INC. Effective date: 20121004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120731 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120731 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120731 |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| R26 | Opposition filed (corrected) |
Opponent name: NOVELIS, INC. Effective date: 20121004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120104 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120729 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20150623 Year of fee payment: 11 Ref country code: FR Payment date: 20150626 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20150721 Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R064 Ref document number: 502005012285 Country of ref document: DE Ref country code: DE Ref legal event code: R103 Ref document number: 502005012285 Country of ref document: DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PT Payment date: 20150727 Year of fee payment: 11 Ref country code: GB Payment date: 20150721 Year of fee payment: 11 Ref country code: CZ Payment date: 20150728 Year of fee payment: 11 Ref country code: ES Payment date: 20150728 Year of fee payment: 11 Ref country code: DE Payment date: 20150721 Year of fee payment: 11 |
|
| RDAF | Communication despatched that patent is revoked |
Free format text: ORIGINAL CODE: EPIDOSNREV1 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20150722 Year of fee payment: 11 Ref country code: HU Payment date: 20150721 Year of fee payment: 11 Ref country code: SE Payment date: 20150721 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20150727 Year of fee payment: 11 |
|
| RDAG | Patent revoked |
Free format text: ORIGINAL CODE: 0009271 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT REVOKED |
|
| 27W | Patent revoked |
Effective date: 20151023 |
|
| GBPR | Gb: patent revoked under art. 102 of the ep convention designating the uk as contracting state |
Effective date: 20151023 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MP4A Effective date: 20160406 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MA03 Ref document number: 540132 Country of ref document: AT Kind code of ref document: T Effective date: 20151023 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: ECNC |