EP1301427B1 - Abklebewerkzeug und verfahren zum automatisierten, serienmässigen applizieren von klebeband - Google Patents
Abklebewerkzeug und verfahren zum automatisierten, serienmässigen applizieren von klebeband Download PDFInfo
- Publication number
- EP1301427B1 EP1301427B1 EP01965093A EP01965093A EP1301427B1 EP 1301427 B1 EP1301427 B1 EP 1301427B1 EP 01965093 A EP01965093 A EP 01965093A EP 01965093 A EP01965093 A EP 01965093A EP 1301427 B1 EP1301427 B1 EP 1301427B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- adhesive tape
- holding device
- application
- masking tool
- applicator roller
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000002390 adhesive tape Substances 0.000 title claims abstract description 107
- 238000000034 method Methods 0.000 title claims abstract description 15
- 239000000853 adhesive Substances 0.000 title claims abstract description 11
- 230000001070 adhesive effect Effects 0.000 title claims abstract description 10
- 230000000873 masking effect Effects 0.000 claims description 29
- 238000005520 cutting process Methods 0.000 claims description 12
- 239000011248 coating agent Substances 0.000 claims description 5
- 238000000576 coating method Methods 0.000 claims description 5
- 239000000463 material Substances 0.000 claims description 5
- 238000000926 separation method Methods 0.000 claims 2
- 238000003825 pressing Methods 0.000 abstract description 11
- 230000000977 initiatory effect Effects 0.000 abstract description 4
- 238000010586 diagram Methods 0.000 description 2
- 239000011888 foil Substances 0.000 description 2
- 239000003292 glue Substances 0.000 description 2
- 230000001681 protective effect Effects 0.000 description 2
- 238000011144 upstream manufacturing Methods 0.000 description 2
- 239000002313 adhesive film Substances 0.000 description 1
- 238000007664 blowing Methods 0.000 description 1
- 230000008021 deposition Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 238000002955 isolation Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000012354 overpressurization Methods 0.000 description 1
- 239000003973 paint Substances 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H35/00—Delivering articles from cutting or line-perforating machines; Article or web delivery apparatus incorporating cutting or line-perforating devices, e.g. adhesive tape dispensers
- B65H35/0006—Article or web delivery apparatus incorporating cutting or line-perforating devices
- B65H35/0013—Article or web delivery apparatus incorporating cutting or line-perforating devices and applying the article or the web by adhesive to a surface
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2801/00—Application field
- B65H2801/51—Automobile
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/10—Methods of surface bonding and/or assembly therefor
- Y10T156/1052—Methods of surface bonding and/or assembly therefor with cutting, punching, tearing or severing
- Y10T156/1084—Methods of surface bonding and/or assembly therefor with cutting, punching, tearing or severing of continuous or running length bonded web
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/10—Methods of surface bonding and/or assembly therefor
- Y10T156/1052—Methods of surface bonding and/or assembly therefor with cutting, punching, tearing or severing
- Y10T156/1084—Methods of surface bonding and/or assembly therefor with cutting, punching, tearing or severing of continuous or running length bonded web
- Y10T156/1085—One web only
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/12—Surface bonding means and/or assembly means with cutting, punching, piercing, severing or tearing
- Y10T156/1348—Work traversing type
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/17—Surface bonding means and/or assemblymeans with work feeding or handling means
- Y10T156/1788—Work traversing type and/or means applying work to wall or static structure
- Y10T156/1793—Grip or clamp for web end
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/17—Surface bonding means and/or assemblymeans with work feeding or handling means
- Y10T156/1788—Work traversing type and/or means applying work to wall or static structure
- Y10T156/1795—Implement carried web supply
Definitions
- the present invention relates to a masking tool for automated, standard application of adhesive tape, in particular on surface parts of vehicle bodies, as well a method for automated, standard application of adhesive tape by means of a robot-controlled generic Abklebetechnikmaschines according to the preambles of claims 1 and 8, as both from the genre forming underlying JP 06211410 A discloses as known.
- the masking tool has a holder for a Adhesive tape roll with adhesive tape to be applied, an applicator roll for attaching peeled from the adhesive tape roll Adhesive tape and one of the Applizierwalze upstream holding device for keeping ready withdrawn from the adhesive tape roll Adhesive tape between two Appliziervor réellen, wherein the Holding device also for pressing held by Adhesive tape on the surface to be glued for initiation an Appliziervorganges serves.
- a takeover provided by means of the of the holding device pressed adhesive tape after advancing the Abklebewerkmaschinees through the applicator roll, which is substantially perpendicular to the plane of the pressed-on adhesive tape in the direction (y) of Tape is extendable.
- the glue tool is used by the Adhesive tape roll peeled tape by means of the holding device the Abklebetechnikmaschinees on a surface to be glued pressed and lifted the holding on the holding device.
- the masking tool will be a few centimeters in the direction of sticking (x) moves, the applicator downstream of the holding device the Abklebetechnikmaschinees in the direction (y) of the tape extended until the applicator roll the tape beaufillon and pressed to the surface to be bonded. Further the masking tool will be the desired length of the sticker moved, wherein the holding device in the area holding the holding device lying tape portion.
- the Adhesive tape is then between holding device and Applizierwalze cut through and the applicator roller (28) re
- the pressure roller is advantageously suspended prancing to the to achieve the necessary contact pressure, the body contour optimal to be able to follow and compensate body tolerances.
- the tape with the Cutting unit accurately cut and the cut-off is by further forward driving the pressure roller pressed.
- the tape gripper grips the beginning of the tape of the next required band and the application cycle begins again.
- the holding device an investment and Andschreib Construction on, at the of Adhesive tape roll applied adhesive tape and by means of a pressing of the adhesive tape on the surface to be bonded to Initiation of a Appliziervorganges done.
- the investment and Andschreib the holding device several Vacuum openings and a coating Made of flexible, flexible material such as soft rubber on.
- a cutting device which is substantially perpendicular to the plane of the adhesive tape in an adhesive tape acting and severing position is adjustable.
- the cutting device comprises a heatable wire.
- the Pressing force with which the adhesive tape on the adhering body section is pressed varied in size or controllable.
- the control of the contact pressure is advantageously carried out depending on the respective requirement of the Adhesive bond, i. Adhesive strength of the adhesive tape to be applied, Surface texture of the adhered body section u.
- the control of the contact force takes place preferably via a proportional valve via the robot controller is controlled.
- Fig. 1 shows a highly schematic diagram of a Inventive Abklebetechnikmaschines for illustration its operation
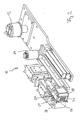
- Fig. 2 is a perspective Representation of a Abklebetechnikmaschines invention (without inserted tape roll) shows.
- the masking tool 10 comprises a holder 12 for an adhesive tape roll 14 and a pressure roller 16, the with inserted adhesive tape roll 14 this on the lateral surface (at parallel central axes) acted upon and the defined Removing of adhesive tape from the adhesive tape roll 14 is used. From the adhesive tape roll 14 withdrawn adhesive tape 15 is so to the pressure roller 16 and about a downstream guide and guide roller 18 steered that the adhesive side of the Adhesive tapes 15 to the outside, i. away from the masking tool 10 has.
- the adhesive tape 15 is deflected and guided in front of a holding device 20, in which it is a vacuum or vacuum unit.
- the to Adhesive tape 15 facing side of the holding device 20 is as Investment and Andschreib Chemistry 22 formed, which is a coating made of flexible, flexible material (such as Soft rubber) and provided in the plurality of openings are, by which a negative pressure of the before Investment and Andschreibfiguration 22 guided adhesive tape 15 takes place.
- one of the holding device 20 (in the removal direction the adhesive tape) downstream applicator roller 28 is provided.
- the Applizierwalze 28 serves to roll the adhesive tape on a surface to be bonded, in particular a surface part a motor vehicle body.
- a cutting device 24 is provided, which at her to the adhesive tape 15 end facing a heatable wire 26th includes.
- Both the applicator roller 28 and the cutter 24 are in the y-direction of the robot coordinate system (cf. Fig. 1), i. in the direction perpendicular to the plane at the Holding device 20 held adhesive tape, free to move adjustable.
- the holding device is also 20 made adjustable in this direction.
- Adhesive tape 15 to the pressure roller 16 and the Whysund Deflection pulley 18 in front of the holding device 20 over until the point indicated by the arrow P in FIG. 1 below the cutting device 24 and is guided by the Holding device 20 by means of vacuum or vacuum held on the investment and Andschreibfiguration 22.
- the robot arm sets the Abklebetechnikmaschine 10 in the y-direction so on the glued Surface on that the tape 15 below the plant and Pressing surface 22 placed on the surface to be bonded is and sticks there. Due to the coating of the plant and Pressing surface with a flexible, flexible material a slight pressure can be exerted by the robot, without causing damage to the surface to be bonded. In addition, surface tolerances can be achieved in this way be balanced in the surface to be stuck.
- the vacuum or vacuum application the holding device 20 is turned off, so that the adhesive tape 15th is no longer held on the investment and Andschreib construction.
- Improving the "release effect" can be a pressure reversal, for example in the form of slight overpressurization or Blowing done.
- the robot moves the masking tool 10 in the direction of adhesion, i.e. essentially in the x direction, along the pasted surface.
- This movement is just about a few inches, for as long as the applicator roller 28 located above the glued tape.
- the holding device 20 downstream Applizierwalze 28 extended in the direction of the tape until it is the tape 15 and applied to the surface to be bonded suppressed.
- the mobility of the applicator roller 28 is shown in FIG. 1 illustrated by the double arrow.
- the Extending the applicator roller 28 is set so that the Applizierwalze 28 further protrudes in its end position as the contact and pressing surface 22 of the holding device 20th This is achieved either by the application roller 28 is extended by a corresponding distance, or thereby, that the holding device 20 is moved back slightly, if it is - as described above - made adjustable.
- the masking tool 10 will be the desired one Length of the sticker moved in the direction of sticking, the Applicator 28, which advantageously has a soft coating has, the adhesive tape 15 on the surface to be bonded imprints.
- the robot tends to prefer the masking tool such that the guide and deflection roller 18 with respect to the Applizierwalze 28 is raised, and the holding function of the holding device 20 is by switching on the vacuum activated again.
- the cutting device moves 24 in the y-direction (see double arrow), i.e. substantially perpendicular to the plane of the adhesive tape, in a the adhesive tape 15 acting and severing Position, wherein the severing by heating the Wire 26 is achieved, and then moves back.
- the last step of the application process is the end of the applied adhesive tape section with the Applizierwalze 28 firmly rolled and the Applizierwalze 28 is retracted again.
- the inventive design of a Abklebewerkmaschines allowed a simplified structure, as the holding and pressing the adhesive tape with a single holding device with combination function he follows. In particular, no separate Means for holding, gripping and feeding the free adhesive tape end to an applicator necessary.
- the simplified structure the masking tool according to the invention also leads to a Simplification of the Appliziervorgangs, in particular the Times between two application processes can be shortened, because the free tape end is already on the pressure surface located with it on the surface to be stuck is pressed.
- the Abklebewerkmaschinemaschine invention allows thus a time-optimized, process-safe automated Applicating tapes, especially adhesive tapes, too on sensitive surfaces.
Landscapes
- Adhesive Tape Dispensing Devices (AREA)
- Details Or Accessories Of Spraying Plant Or Apparatus (AREA)
- Folding Of Thin Sheet-Like Materials, Special Discharging Devices, And Others (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
- Coating Apparatus (AREA)
Abstract
Description
- Aufdrücken von von einer Klebebandrolle abgezogenem Klebeband auf eine zu beklebende Oberfläche mittels einer Halteeinrichtung des Abklebewerkzeugs,
- Beenden des Haltens des Klebebands an der Halteeinrichtung,
- Bewegen des Abklebewerkzeugs um einige Zentimeter in Beklebungsrichtung,
- Ausfahren einer der Halteeinrichtung nachgeordneten Applizierwalze des Abklebewerkzeugs in Richtung des Klebebands bis die Applizierwalze das Klebeband beaufschlägt und an die zu beklebende Oberfläche drückt,
- Bewegen des Abklebewerkzeugs um die gewünschte Länge der Beklebung,
- Neigen des Abklebewerkzeugs,
- Wiederaufnehmen des Haltens durch die Halteeinrichtung von im Bereich der Halteeinrichtung liegendem Klebeband,
- Durchtrennen des Klebebands zwischen Halteeinrichtung und Applizierwalze,
- Einfahren der Applizierwalze,
- Fig. 1
- zeigt eine stark schematisierte Prinzipdarstellung eines erfindungsgemäßen Abklebewerkzeugs in Draufsicht.
- Fig. 2
- zeigt eine perspektivische Darstellung eines erfindungsgemäßen Abklebewerkzeugs ohne eingelegte Klebebandrolle.
Claims (9)
- Abklebewerkzeug (10) zum automatisierten, serienmäßigen Applizieren von Klebeband, insbesondere auf Oberflächenpartien von Fahrzeug-Karosserien, mit einer Halterung (12) für eine Klebebandrolle (14) mit zu applizierendem Klebeband (15), einer Applizierwalze (28) zum Anbringen von von der Klebebandrolle (14), abgezogenem Klebeband (15) und einer der Applizierwalze (28) vorgeordneten Halteeinrichtung (20) zum Bereithalten von von der Klebebandrolle (14) abgezogenem Klebeband (15) zwischen zwei Appliziervorgängen, wobei die Halteeinrichtung (20) darüber hinaus zum Andrücken von bereitgehaltenem Klebeband (15) auf der zu beklebenden Oberfläche zum Einleiten eines Appliziervorganges dient und eine Übernahme von von der Halteeinrichtung (20) angedrücktem Klebeband nach Vorwärtsbewegen des Abklebewerkzeuges (10) durch die Applizierwalze (28) erfolgt, die im wesentlichen senkrecht zu der Ebene des angedrückten Klebebands (15) in Richtung (y) des Klebebandes ausfahrbar ist,
dadurch gekennzeichnet, dass die Halteeinrichtung (20) das Klebeband (15) mittels Unterdruckbeaufschlagung hält. - Abklebewerkzeug nach Anspruch 1,
dadurch gekennzeichnet, dass die Halteeinrichtung (20) eine Anlage- und Andrückfläche (22) aufweist, an der von der Klebebandrolle (14) abgezogenes Klebeband (15) anliegt und mittels der ein Andrücken des Klebebands (15) auf der zu beklebenden Oberfläche zum Einleiten eines Appliziervorganges erfolgt. - Abklebewerkzeug nach Anspruch 2,
dadurch gekennzeichnet, dass Mittel zur Steuerung der Anpreßkraft des Klebebands (15) vorgesehen sind. - Abklebewerkzeug nach Anspruch 3,
dadurch gekennzeichnet, dass die Steuerung der Anpreßkraft über ein Proportionalventil erfolgt. - Abklebewerkzeug nach einem der Ansprüche 2 bis 4,
dadurch gekennzeichnet, dass die Anlage- und Andrückfläche (22) mehrere Öffnungen zur Unterdruckbeaufschlagung sowie eine Beschichtung aus nachgiebigem, flexiblem Material wie Weichgummi aufweist. - Abklebewerkzeug nach einem der Ansprüche 1 bis 5,
dadurch gekennzeichnet, dass eine zwischen Halteeinrichtung (20) und Applizierwalze (28) angeordnete Schneideinrichtung (24) vorgesehen ist, die im wesentlichen senkrecht zur Ebene des Klebebandes in eine das Klebeband (15) beaufschlagende und durchtrennende Position verstellbar ist. - Abklebewerkzeug nach Anspruch 6,
dadurch gekennzeichnet, dass die Schneideinrichtung (24) einen aufheizbaren Draht (26) umfaßt. - Verfahren zum automatisierten, serienmäßigen Applizieren von Klebeband, insbesondere auf Oberflächenpartien von Fahrzeug-Karosserien, mittels eines robotergesteuerten Abklebewerkzeuges (10) insbesondere nach einem der Ansprüche 1 bis 7, bei dem von einer Klebebandrolle (14) abgezogenes Klebeband (15) mittels einer Halteeinrichtung (20) des Abklebewerkzeuges (10) auf eine zu beklebende Oberfläche aufgedrückt und das Halten an der Halteeinrichtung (20) aufgehoben wird, das Abklebewerkzeug einige Zentimeter in Beklebungsrichtung (x) bewegt wird, eine der Halteeinrichtung (20) nachgeordnete Applizierwalze (28) des Abklebewerkzeuges (10) in Richtung (y) des Klebebandes (15) ausgefahren wird, bis die Applizierwalze (28) das Klebeband beaufschlägt und an die zu beklebende Oberfläche drückt, das Abklebewerkzeug (10) um die gewünschte Länge der Beklebung bewegt wird und die Halteeinrichtung (20) einen im Bereich der Halteeinrichtung (20) liegenden Klebebandabschnitt hält, das Klebeband (15) zwischen Halteeinrichtung (20) und Applizierwalze (28) durchtrennt und die Applizierwalze (28) wieder eingefahren wird,
dadurch gekennzeichnet, dass das Klebeband (15) von der Halteeinrichtung (20) mittels Unterdruckbeaufschlagung gehalten wird und dass das Abklebewerkzeug (10) vor dem Durchtrennen des Klebebandes (15) geneigt wird. - Verfahren nach Anspruch 8,
dadurch gekennzeichnet, dass nach dem Durchtrennen des Klebebandes und vor dem Einfahren der Applizierwalze (28) das Ende des applizierten Klebebandabschnittes mit der Applizierwalze (28) festgewalzt wird.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10035236A DE10035236A1 (de) | 2000-07-20 | 2000-07-20 | Abklebewerkzeuge und Verfahren zum automatisierten, serienmäßigen Applizieren von Klebeband |
| DE10035236 | 2000-07-20 | ||
| PCT/EP2001/007868 WO2002008102A2 (de) | 2000-07-20 | 2001-07-07 | Abklebewerkzeug und verfahren zum automatisierten, serienmässigen applizieren von klebeband |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1301427A2 EP1301427A2 (de) | 2003-04-16 |
| EP1301427B1 true EP1301427B1 (de) | 2003-12-17 |
Family
ID=7649546
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01965093A Expired - Lifetime EP1301427B1 (de) | 2000-07-20 | 2001-07-07 | Abklebewerkzeug und verfahren zum automatisierten, serienmässigen applizieren von klebeband |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US7001478B2 (de) |
| EP (1) | EP1301427B1 (de) |
| JP (1) | JP3782777B2 (de) |
| DE (2) | DE10035236A1 (de) |
| ES (1) | ES2211825T3 (de) |
| WO (1) | WO2002008102A2 (de) |
Families Citing this family (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US8000837B2 (en) * | 2004-10-05 | 2011-08-16 | J&L Group International, Llc | Programmable load forming system, components thereof, and methods of use |
| US20090226516A1 (en) * | 2008-03-04 | 2009-09-10 | Pharma Pass Ii Llc | Sartan compositions |
| JP2016124673A (ja) * | 2015-01-05 | 2016-07-11 | スリーエム イノベイティブ プロパティズ カンパニー | 貼付装置、物品及び貼付方法 |
| CN108946279B (zh) * | 2018-07-31 | 2024-03-26 | 杭州奥方科技有限公司 | 胶带贴合器 |
| DE102018218283A1 (de) | 2018-09-11 | 2020-03-12 | Tesa Se | Verfahren zum Aufbringen von Stanzteilen auf Oberflächen sowie Testverfahren dafür |
| DE102019215943A1 (de) | 2019-10-16 | 2021-04-22 | Tesa Se | Verfahren zum automatisierten Entfernen einer Lackier-Schutzfolie von mindestens einem Teil einer Karosserie |
| CN117157240A (zh) * | 2021-04-08 | 2023-12-01 | 3M创新有限公司 | 表面表征模块和包括表面表征模块的系统 |
| JP2024520226A (ja) * | 2021-04-08 | 2024-05-23 | スリーエム イノベイティブ プロパティズ カンパニー | 表面特徴判定モジュール及びそれを含むシステム |
| CN116215962B (zh) * | 2023-03-31 | 2025-09-16 | 苏州华兴源创科技股份有限公司 | 覆膜工艺及覆膜装置 |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0193626A1 (de) * | 1985-03-02 | 1986-09-10 | SUNDEVED Maskinfabrik A/S | Vorrichtung zum Aufbringen eines Aufreissbandes oder dergleichen auf Wellpappen-, Pappen-, Papierbahnen o. dgl. |
| JPH06211410A (ja) * | 1993-01-14 | 1994-08-02 | Lintec Corp | テープ貼付ヘッドおよびテープ自動貼付装置 |
| JP3487681B2 (ja) * | 1994-11-25 | 2004-01-19 | 積水化学工業株式会社 | 封緘機などにおける包装テープの貼付装置 |
| GB2325453A (en) * | 1997-05-21 | 1998-11-25 | Eastman Kodak Co | Tape Applying Device With Non-Driven Vacuum Roller |
| JPH11193172A (ja) | 1998-01-05 | 1999-07-21 | San Tec:Kk | 粘着シートの貼付装置 |
| DE19809515C2 (de) * | 1998-03-05 | 2002-10-31 | Daimler Chrysler Ag | Verfahren und Vorrichtung zum Applizieren von selbsthaftender Schutzfolie auf Karosserien |
-
2000
- 2000-07-20 DE DE10035236A patent/DE10035236A1/de not_active Withdrawn
-
2001
- 2001-07-07 US US10/333,263 patent/US7001478B2/en not_active Expired - Fee Related
- 2001-07-07 WO PCT/EP2001/007868 patent/WO2002008102A2/de not_active Ceased
- 2001-07-07 ES ES01965093T patent/ES2211825T3/es not_active Expired - Lifetime
- 2001-07-07 EP EP01965093A patent/EP1301427B1/de not_active Expired - Lifetime
- 2001-07-07 JP JP2002513805A patent/JP3782777B2/ja not_active Expired - Fee Related
- 2001-07-07 DE DE50101211T patent/DE50101211D1/de not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| US20040026026A1 (en) | 2004-02-12 |
| ES2211825T3 (es) | 2004-07-16 |
| WO2002008102A2 (de) | 2002-01-31 |
| DE10035236A1 (de) | 2002-01-31 |
| WO2002008102A3 (de) | 2002-11-28 |
| US7001478B2 (en) | 2006-02-21 |
| JP2004504238A (ja) | 2004-02-12 |
| EP1301427A2 (de) | 2003-04-16 |
| JP3782777B2 (ja) | 2006-06-07 |
| DE50101211D1 (de) | 2004-01-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1519829B1 (de) | Verfahren und vorrichtung zum automatisierten applizieren von lackfolie auf karosserieteile sowie automationsgerecht gestalteter lackfolienverbund | |
| EP1058649B1 (de) | Verfahren und vorrichtung zum applizieren von selbsthaftender schutzfolie auf karosserien | |
| DE10339067B4 (de) | Verfahren und Vorrichtung zum automatisierten Applizieren von Lackfolie auf Karosserieteile | |
| EP0771300B1 (de) | Verfahren und vorrichtung zum vorbereiten eines anfanges einer vorratspapierbahnrolle für einen fliegenden rollenwechsel | |
| EP0450312A1 (de) | Verfahren zum Verbinden des Bahnanfanges eines Wickels an einer Splice-Stelle mit dem Bahnende einer von einem anderen Wickel ablaufenden Bahn | |
| EP0838398A1 (de) | Verfahren und Vorrichtung zum Applizieren von selbsthaftender Schutzfolie auf Karosserien | |
| EP1263567B1 (de) | Verfahren und vorrichtung zum aufbringen von selbstklebenden folienzuschnitten, insbesondere auf kfz-karosserieteile | |
| CH683829A5 (de) | Verfahren zum Herstellen eines Wabenkerns aus einer bandförmigen Folie, Vorrichtung zur Durchführung des Verfahrens und Verwendung des Wabenkerns für Verbundplatten. | |
| DE102018217921A1 (de) | Applikationseinheit und Verfahren zur Verarbeitung von selbstklebenden Stanzteilen zum Verschluss von Öffnungen in einem Fahrzeugelement | |
| DE10311267B4 (de) | Verfahren und Vorrichtung zum automatisierten Applizieren von Lackfolie auf Karosserieteile und Verwendung eines ausgespannten Haftklebebandes dabei | |
| EP0388398B1 (de) | Vorrichtung zum Abnehmen eines flächigen Werkstückes von einer anklebenden Unterfolie | |
| DE10035236A1 (de) | Abklebewerkzeuge und Verfahren zum automatisierten, serienmäßigen Applizieren von Klebeband | |
| EP2763921A1 (de) | Vorrichtung und verfahren zum bereitstellen von folienblättern, appliziervorrichtung zum bestücken von gegenständen mit folienblättern | |
| DE3443939C2 (de) | Verfahren zum Entfernen der Schutzfolie von mit belichtetem Photoresist laminierten Leiterplatten | |
| DE102008000461B3 (de) | Verfahren und Vorrichtung zum Abziehen einer Folie von einem plattenartigen Trägern oder einer Folie | |
| DE4033834A1 (de) | Verfahren zum herstellen eines ununterbrochenen aufkleberblattes | |
| DE1911615A1 (de) | Vorrichtung zum Auftragen einer doppelseitigen Haftklebefolie | |
| DE102004000040A1 (de) | Vorrichtung und Verfahren zum Einlegen einer Wickelhülse | |
| DE102004021622B3 (de) | Vorrichtung und ein Verfahren zum Aufbringen eines Klebebandes | |
| EP0977688A1 (de) | Appliziervorrichtung sowie applizierverfahren für linerless-etiketten | |
| AT401634B (de) | Verfahren und vorrichtung zum herstellen eines verbundwerkstückes | |
| DE1263474B (de) | Verfahren zum Herstellen eines mit Selbstklebeetiketten versehenen Vorratstraegers | |
| DE19729026C1 (de) | Verfahren und Vorrichtung zum Aufkleben eines von einer Vorratsrolle abgezogenen und abgelängten Abschnittes eines Klebebandes | |
| WO1996036482A1 (de) | Vorrichtung und verfahren zum luftdichten verkleben von folienschläuchen | |
| WO1988004981A1 (fr) | Procede et dispositif pour enlever un film protecteur |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20021223 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT SE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50101211 Country of ref document: DE Date of ref document: 20040129 Kind code of ref document: P |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20040223 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20031217 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2211825 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040920 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20090724 Year of fee payment: 9 Ref country code: FR Payment date: 20090716 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20090720 Year of fee payment: 9 Ref country code: SE Payment date: 20090715 Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD Ref country code: FR Ref legal event code: CA |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20090725 Year of fee payment: 9 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20100707 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20110331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100707 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100802 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100707 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20110818 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100708 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100708 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20121001 Year of fee payment: 12 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140201 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50101211 Country of ref document: DE Effective date: 20140201 |