EP1240474B1 - Geschoss und verfahren zur fertigung eines geschosses - Google Patents
Geschoss und verfahren zur fertigung eines geschosses Download PDFInfo
- Publication number
- EP1240474B1 EP1240474B1 EP00979324A EP00979324A EP1240474B1 EP 1240474 B1 EP1240474 B1 EP 1240474B1 EP 00979324 A EP00979324 A EP 00979324A EP 00979324 A EP00979324 A EP 00979324A EP 1240474 B1 EP1240474 B1 EP 1240474B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- projectile
- guide
- projectile body
- guide means
- protrusions
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004519 manufacturing process Methods 0.000 title claims description 13
- 239000000835 fiber Substances 0.000 claims abstract description 39
- 239000002131 composite material Substances 0.000 claims abstract description 11
- 238000000034 method Methods 0.000 claims abstract description 8
- 238000010304 firing Methods 0.000 claims abstract description 6
- 239000000463 material Substances 0.000 claims description 8
- 230000002787 reinforcement Effects 0.000 claims description 3
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims 2
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims 1
- RTAQQCXQSZGOHL-UHFFFAOYSA-N Titanium Chemical compound [Ti] RTAQQCXQSZGOHL-UHFFFAOYSA-N 0.000 claims 1
- 239000000654 additive Substances 0.000 claims 1
- 238000004026 adhesive bonding Methods 0.000 claims 1
- 229910052799 carbon Inorganic materials 0.000 claims 1
- 210000001520 comb Anatomy 0.000 claims 1
- 229910052759 nickel Inorganic materials 0.000 claims 1
- 239000010936 titanium Substances 0.000 claims 1
- 229910052719 titanium Inorganic materials 0.000 claims 1
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 abstract description 15
- 229910052802 copper Inorganic materials 0.000 abstract description 14
- 239000010949 copper Substances 0.000 abstract description 14
- 239000007789 gas Substances 0.000 abstract description 5
- 239000003380 propellant Substances 0.000 abstract 1
- 238000011161 development Methods 0.000 description 8
- 238000013461 design Methods 0.000 description 6
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 description 4
- 229910052751 metal Inorganic materials 0.000 description 3
- 239000002184 metal Substances 0.000 description 3
- 238000007789 sealing Methods 0.000 description 3
- 239000010425 asbestos Substances 0.000 description 2
- 239000004744 fabric Substances 0.000 description 2
- 230000002349 favourable effect Effects 0.000 description 2
- 239000002657 fibrous material Substances 0.000 description 2
- 239000000945 filler Substances 0.000 description 2
- 239000007788 liquid Substances 0.000 description 2
- 150000002739 metals Chemical class 0.000 description 2
- 229910052757 nitrogen Inorganic materials 0.000 description 2
- 239000004810 polytetrafluoroethylene Substances 0.000 description 2
- 229920001343 polytetrafluoroethylene Polymers 0.000 description 2
- 229910052895 riebeckite Inorganic materials 0.000 description 2
- 239000004753 textile Substances 0.000 description 2
- 238000004804 winding Methods 0.000 description 2
- 229920000049 Carbon (fiber) Polymers 0.000 description 1
- ZOKXTWBITQBERF-UHFFFAOYSA-N Molybdenum Chemical compound [Mo] ZOKXTWBITQBERF-UHFFFAOYSA-N 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- 230000001133 acceleration Effects 0.000 description 1
- 239000011230 binding agent Substances 0.000 description 1
- 239000004917 carbon fiber Substances 0.000 description 1
- 125000002915 carbonyl group Chemical group [*:2]C([*:1])=O 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000002474 experimental method Methods 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 239000000314 lubricant Substances 0.000 description 1
- 239000007769 metal material Substances 0.000 description 1
- 229910052750 molybdenum Inorganic materials 0.000 description 1
- 239000011733 molybdenum Substances 0.000 description 1
- 230000000149 penetrating effect Effects 0.000 description 1
- 239000000843 powder Substances 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 230000000750 progressive effect Effects 0.000 description 1
- 238000007493 shaping process Methods 0.000 description 1
- 230000006641 stabilisation Effects 0.000 description 1
- 238000011105 stabilization Methods 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 229920003002 synthetic resin Polymers 0.000 description 1
- 239000000057 synthetic resin Substances 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
- 229920002725 thermoplastic elastomer Polymers 0.000 description 1
- 229920001187 thermosetting polymer Polymers 0.000 description 1
- 238000012549 training Methods 0.000 description 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 1
Images

Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F42—AMMUNITION; BLASTING
- F42B—EXPLOSIVE CHARGES, e.g. FOR BLASTING, FIREWORKS, AMMUNITION
- F42B14/00—Projectiles or missiles characterised by arrangements for guiding or sealing them inside barrels, or for lubricating or cleaning barrels
- F42B14/02—Driving bands; Rotating bands
Definitions
- the invention relates to a projectile according to the preamble of claim 1 and a method for its production according to claim 13.
- Known projectiles usually have one on the outer surface of the bullet body fastened guide means made of copper on. There are also floors with several at a defined distance mutually arranged guide means known. These guide means are in the form of ring-shaped elevations educated. When shooting a projectile body designed in this way in a gun barrel, the inner surface of which has several spirally circumferential grooves the elevations are pressed in and shaped, creating the projectile undergoes a rotation, resulting in its stabilization serves on its trajectory. At the same time, the guide means works to seal against the on the rear side of the floor hot powder gases and as friction-reducing Intermediate layer between the floor and Gun barrel.
- a sleeve-shaped, guideband that can be ejected from the projectile Fiber material, preferably asbestos with thermal hardenable synthetic resin is soaked.
- a filler such as PTFE is added to the fiber material in density, which should also serve as a lubricant and / or shattering guide bands are for Precision weapons are not suitable because they have undefined initial conditions create and also limited in their strength so they're not modern weapon systems suffice.
- the sleeve-shaped guide band is also about fasteners like screws etc. connected to the projectile and at least partially experiences one after the shot Disassembly, causing mechanical damage as well a risk from asbestos dust.
- the invention is intended to overcome the disadvantages of the prior art and design a projectile so that when it is fired an entry of copper into the gun barrel and / or other materials in the area largely avoids. Furthermore, the invention is based on the problem a method of manufacturing a projectile like this to further develop the entry of copper into avoid the gun barrel when firing the projectile leaves.
- the first problem is caused by the features of the claim 1 solved.
- the helix angle specified in the patent claim corresponds to that in the inner pipe wall, i.e. the twist angle the trains of the gun barrel from which the projectile was shot becomes.
- the guiding means can be omitted by this design manufacture a copper-free material.
- the inventive Bullet thereby reliably prevents it from being fired an entry of copper into the gun barrel. A This prevents embrittlement of the gun barrel.
- the reduced, necessary for the deformation of the guide means Energy, the resulting lower inguinal forces and Wear also has a favorable effect on the service life of the pipes and allow an increase in range of the floor.
- the manufacturing method according to the invention is very economical and also suitable for mass production.
- the guide band can be made according to another advantageous one Training cost-effectively around the projectile body wrap when the guide tape has a smooth section and a section carrying the elevations of the guide means and that the sections abut each other and are glued together.
- connection of the sections of the guide band is designed according to another advantageous development of the Invention constructively particularly simple if there are fibers of the smooth section over which the elevations of the guide means having section extend.
- connection of overlapping fiber sections has according to an advantageous development of the invention particularly high strength when the surveys each a plurality of layers arranged one above the other Have fiber sections and when the fiber sections are adjacent Intermeshing elevations.
- the areas provided for support on the gun barrel the guide means have according to another advantageous Development of the invention a particularly high stability, if the surveys have deposits for reinforcement.
- the inserts can, for example, consist of short fiber sections consist.
- the smooth section of the guide tape could, for example be glued to the projectile body.
- the leader band is particularly reliable in its intended position held when the smooth section of the guide tape is positively attached to the projectile body.
- the guide band can be like that of the known projectile be ring-shaped.
- a centering of the guide band on the projectile body is particularly simple, if this one in a recess of the projectile body penetrating centering process.
- gas-forming filler materials such as metal carbonyls are created during the launch in the gun barrel resulting frictional heat on the guide gases and expansions that cause increased sealing and thus serve to increase the range of the storeys.
- a combination of guide means made of fiber composite material with those made of copper-free metals results in optimal Sealing and pressure conditions and thermal loads in high-performance guns, especially if that rear, metallic guide means less Has diameter than that arranged in the firing direction made of fiber composite material.
- metallic guide means less Has diameter than that arranged in the firing direction made of fiber composite material.
- the second problem namely a manufacturing process to develop a floor so that it can the entry of copper into the gun barrel when fired of the projectile can be avoided according to the invention the features of claim 13.
- This design allows the use of copper in the area touching the gun barrel when fired of the projectile reliably prevent.
- the floor is manufactured according to a other advantageous development of the invention particularly inexpensive if the guide tape is initially a strip with a smooth section and an elevation of the guide means having section is formed when the smooth section one or more times around the projectile body is led around and when the one showing the surveys Section is glued to the smooth section. hereby the guide band is simply around the projectile body wound.
- the intended dimensions of the guide belt can be according to a further advantageous development of the invention with particularly small tolerances if that Guide tape pressed against the projectile body when glued becomes.
- the pressing of the guide band with the projectile body can, for example, by means of a Guide band pushed ring.
- the guide tape can be rolled up before winding up its sections attach to the projectile body when the free Riveted to the end of the smooth section on the projectile body becomes.
- the guide band can be used independently of the projectile body manufacture and then assemble it, if for fastening an annular, one the diameter the outer diameter corresponding to the groove of the projectile body having the guide band of the projectile body initially is cooled until the guide band over the projectile body can be pushed as far as the groove and then afterwards the projectile body is heated with the guide band becomes.
- Liquid nitrogen in particular can be used for this with which the projectile body moves to minus Can cool at 170 ° C.
- ring-shaped guide bands can be special Produce economically by initially tubular Initial components are manufactured, which are then laser or Water jet cutting process to the required installation length be tailored.
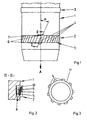
- Figure 1 shows a portion of a floor with a projectile body 1 arranged guide means 2 and with one arranged at a distance from the guide means 2 additional guide ring 3.
- the outer areas of the Guide means 2 are on the shot of the projectile on the inner wall of a gun barrel, not shown on, while the guide ring 3 is only weakly in the spiral shape of the tube engages.
- the guide means 2 has several protruding from the lateral surface of the projectile body 1 Surveys 4.
- the surveys 4 are essentially longitudinal to the projectile body 1 and by a swirl angle ( ⁇ ) arranged inclined to its longitudinal axis.
- the Guide means 2 and the guide ring 3 stabilize the Trajectory of the projectile and generate a predetermined Swirl.
- the elevations 4 of the guide means 2 are on one ring-shaped, made of a fiber composite material Guide belt 5 arranged.
- the guide belt 5 has one Centering extension 6, which is positively in a recess 7 of the projectile body 1 is held.
- the twist angle ( ⁇ ) corresponds to the angle of the trains in the gun barrel, to one to its soul axis (central axis) parallel line.
- a maximum initial acceleration to achieve this angle corresponds ( ⁇ ) the initial twist in the inner tube wall, for example with a progressive twist.
- the launch direction is designated A; in the following Figures are the same parts with the same reference numerals Mistake.
- Figure 2 shows in a greatly enlarged sectional view through the projectile from Figure 1, along the line II - II that the projectile body 1 has a groove 8, which the Guide band 5 holds axially. Furthermore, are shown schematically in FIG Fibers 9 and a binder 10, which the fibers glued together, shown. The fibers 9 are immediate at the outer limits of the guide band 5 arranged. Furthermore, they are tangential and radial Directional fibers 9 at an angle of approximately 45 ° to the longest extension of the guide means 2 arranged.
- FIG 3 shows an annular and closed design Guide belt 11.
- the guide belt 11 can, for example shrunk onto the floor shown in Figure 1 become.
- the projectile body 1 is attached liquid nitrogen cooled down to minus 170 ° C. there the diameter of the projectile body 1 is reduced so far, that the guide band 11 with over the projectile body 1 to the groove 8 shown in Figure 2 are pushed can.
- the projectile body expands 1 off again. After all, is the leader band 11 axially immovable in the groove 8 of the projectile body 1 held.
- Figure 4 shows the projectile from Figure 1 in a plan view in the manufacture of a guide band 12.
- the guide band 12 has a smooth section 13 and one of the elevations 4 having section 14.
- Sections 13, 14 are from pressed together and / or glued fiber mats manufactured.
- the free end of the smooth portion 13 becomes, for example by means of a schematically shown in the drawing Rivets 15 fixed in the groove 8 of the projectile body 1.
- Rivets 15 fixed in the groove 8 of the projectile body 1.
- Figure 5 shows an example of a fiber course of the surveys 4 area of the guide belt 12 Figure 4.
- Have fiber sections 16, 17 of the guide belt 12 a shape corresponding to the surveys 4 and are on the the elevations 4 facing away from the shape of the bottom region the groove 8 of the projectile body shown in Figure 4 1 smooth design. Adjacent fiber sections 16, 17 overlap each other.
- FIG. 6 shows the fiber course of the surveys 4 Area of the guide belt 12 from Figure 4 in a another embodiment.
- This embodiment differs differs from that of Figure 5 mainly in that each other bordering fiber sections 18, 19 intermesh like a comb.
- the elevations have 4 areas forming them of the guide belt 12 deposits 20 for reinforcement on.
- the inserts 20 can of course be like the fiber sections 18, 19 also from pressed together and / or glued fiber mats.
- the guide ring 3 can be used for shorter storeys be omitted or also in the form of a Fiber composite material made analogously to the guide means 2 his.
Landscapes
- Engineering & Computer Science (AREA)
- General Engineering & Computer Science (AREA)
- Aiming, Guidance, Guns With A Light Source, Armor, Camouflage, And Targets (AREA)
- Moulding By Coating Moulds (AREA)
Abstract
Description
- Fig. 1
- einen Teilbereich eines erfindungsgemässen Geschosses,
- Fig. 2
- eine stark vergrösserte Schnittdarstellung durch das Geschoss aus Figur 1 entlang der Linie II - II,
- Fig. 3
- eine Draufsicht auf ein Führungsband für das Geschoss aus Figur 1,
- Fig. 4
- eine schematische Draufsicht auf das Geschoss aus Figur 1 bei einer Fertigung des Führungsbandes durch Wickeln,
- Fig. 5
- eine schematische Darstellung eines Faserverlaufs einer weiteren Ausführungsform des Führungsbandes aus Figur 3,
- Fig. 6
- eine schematische Darstellung eines Faserverlaufs einer weiteren Ausführungsform des Führungsbandes aus Figur 3.
Claims (15)
- Geschoss mit einem Geschosskörper (1) und mit auf diesem Geschosskörper (1) angeordneten radial abstehenden Führungsmitteln (2), aus einem Faserverbundmaterial, zur Führung des Geschosskörpers (1) in einem Geschützrohr, dadurch gekennzeichnet, dass das Faserverbundmaterial Kohlefasern aufweist und dass aus dem Führungsmittel (2) wenigstens eine Erhebung (4) absteht, welche gegenüber der Längsachse des Geschosskörpers (1) um einen Drallwinkel (α) geneigt ist.
- Geschoss nach Anspruch 1, dadurch gekennzeichnet, dass das Führungsmittel (2) bildende Führungsband (5, 11, 12) Matten aus überkreuz gewebten Fasern (9) enthält und dass die Fasern (9) in den Matten um 45° zur Längsachse von langgestreckten Erhebungen (4) des Führungsmittels (2) geneigt angeordnet sind.
- Geschoss nach Anspruch 2, wobei das Führungsband (11, 12) einen glatten Abschnitt (13) und einen die Erhebungen (4) des Führungsmittels (2) tragenden Abschnitt (14) aufweist, dadurch gekennzeichnet, dass und dass die einzelnen Abschnitte (13, 14) aneinander anliegen und miteinander verklebt sind.
- Geschoss nach zumindest einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass sich Fasern des glatten Abschnitts (13) bis über den die Erhebungen (4) des Führungsmittels (2) aufweisenden Abschnitt (14) erstrecken.
- Geschoss nach zumindest einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Erhebungen (4) des Führungsmittels (2) jeweils einzelne, einander überlappenden Faserabschnitte (16-19) aufweisen.
- Geschoss nach zumindest einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Erhebungen (4) jeweils eine Mehrzahl von schichtweise übereinander angeordneten Faserabschnitten (19) aufweisen und dass sich die Faserabschnitte (19) einander benachbarter Erhebungen (4) kammartig übergreifen.
- Geschoss nach zumindest einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass die Erhebungen (4) Einlagen (20) zur Verstärkung aufweisen.
- Geschoss nach zumindest einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass der glatte Abschnitt (13) des Führungsbandes (12) formschlüssig an dem Geschosskörper (1) befestigt ist.
- Geschoss nach zumindest einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass das Führungsband (5) einen in eine Ausnehmung (7) des Geschosskörpers (1) eindringenden Zentrierungsfortsatz (6) aufweist.
- Geschoss nach zumindest einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass ein Zentrierungsfortsatz (6) in Abschussrichtung (A) des Geschosses weisend, angeordnet ist.
- Geschoss nach Anspruch 1, dadurch gekennzeichnet, dass das Faserverbundmaterial, insbesondere seine Erhebungen (4) gasbildende Zusatzwerkstoffe enthalten.
- Geschoss nach zumindest einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass am Geschoss heckseitig zum Führungsmittel (2) resp. zum Führungsband (5) beabstandet, wenigstens ein weiteres Führungsband (3) angeordnet ist, welches einen geringeren Durchmesser als das abschussseitige aufweist und aus Nickel oder Titan besteht.
- Verfahren zur Fertigung eines Geschosses nach einem der Ansprüche 1-12, bei dem ein Führungsmittel aufweisendes Führungsband in einer entsprechend gestalteten Nut eines Geschosskörpers befestigt wird, dadurch gekennzeichnet, dass das Führungsband zunächst als Streifen mit einem glatten Abschnitt und einen Erhebungen der Führungsmittel aufweisenden Abschnitt geformt wird, dass der glatte Abschnitt ein oder mehrmals um den Geschosskörper herumgeführt wird und dass der die Erhebungen aufweisende Abschnitt mit dem glatten Abschnitt verklebt wird, wobei das Führungsband beim Verkleben gegen den Geschosskörper gepresst wird.
- Verfahren nach Anspruch 13, dadurch gekennzeichnet, dass das freie Ende des glatten Abschnitts an dem Geschosskörper festgenietet wird.
- Verfahren zur Fertigung eines Geschosses nach einem der Ansprüche 1-12 bei dem ein Führungsmittel aufweisendes Führungsband in einer entsprechend gestalteten Nut eines Geschosskörpers befestigt wird, dadurch gekennzeichnet, dass zur Befestigung des ringförmigen, einen dem Durchmesser der Nut des Geschosskörpers entsprechenden Aussendurchmesser aufweisenden Führungsbandes der Geschosskörper zunächst soweit gekühlt wird, bis sich das Führungsband über den Geschosskörper bis zu der Nut schieben lässt und, dass anschliessend der Geschosskörper mit dem Führungsband erwärmt wird.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP00979324A EP1240474B1 (de) | 1999-12-20 | 2000-12-18 | Geschoss und verfahren zur fertigung eines geschosses |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP99811177A EP1111329A1 (de) | 1999-12-20 | 1999-12-20 | Geschoss und Verfahren zur Fertigung eines Geschosses |
| EP99811177 | 1999-12-20 | ||
| PCT/CH2000/000669 WO2001046640A1 (de) | 1999-12-20 | 2000-12-18 | Geschoss und verfahren zur fertigung eines geschosses |
| EP00979324A EP1240474B1 (de) | 1999-12-20 | 2000-12-18 | Geschoss und verfahren zur fertigung eines geschosses |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1240474A1 EP1240474A1 (de) | 2002-09-18 |
| EP1240474B1 true EP1240474B1 (de) | 2003-10-01 |
Family
ID=8243201
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99811177A Withdrawn EP1111329A1 (de) | 1999-12-20 | 1999-12-20 | Geschoss und Verfahren zur Fertigung eines Geschosses |
| EP00979324A Expired - Lifetime EP1240474B1 (de) | 1999-12-20 | 2000-12-18 | Geschoss und verfahren zur fertigung eines geschosses |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99811177A Withdrawn EP1111329A1 (de) | 1999-12-20 | 1999-12-20 | Geschoss und Verfahren zur Fertigung eines Geschosses |
Country Status (4)
| Country | Link |
|---|---|
| EP (2) | EP1111329A1 (de) |
| AU (1) | AU1686501A (de) |
| DE (1) | DE50003951D1 (de) |
| WO (1) | WO2001046640A1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR102960603B1 (ko) * | 2025-03-05 | 2026-04-30 | 김준규 | 무게중심이 전방에 위치한 탄두체 및 안정화된 탄도 특성을 위한 가이드링 구조를 이용한 탄도 안정화 방법 및 장치. |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| RU2260168C2 (ru) * | 2003-04-04 | 2005-09-10 | Иркутский военный авиационный инженерный институт | Малокалиберный артиллерийский снаряд с полимерными ведущими устройствами |
| USD689975S1 (en) | 2012-01-16 | 2013-09-17 | Alliant Techsystems Inc. | Practice projectile |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR5398E (fr) * | 1904-04-20 | 1906-03-27 | Krupp Ag | Projectile en acier avec évidement rempli d'un métal à poids spécifique élevé |
| US2699094A (en) * | 1947-02-19 | 1955-01-11 | Musser Clarence Walton | Rifled firearm which automatically indexes preengraved projectiles |
| US3130671A (en) * | 1955-11-26 | 1964-04-28 | Berghaus Elektrophysik Anst | Method of reducing barrel wear |
| GB1164299A (en) * | 1966-10-25 | 1969-09-17 | Henry Crossley Packings Ltd | Projectile Driving Bands. |
| GB1236694A (en) * | 1969-05-23 | 1971-06-23 | Henry Crossley Packings Ltd | Projectile driving bands |
| US3738279A (en) * | 1970-07-24 | 1973-06-12 | Us Navy | Sabot for sub-calibre projectile |
| US3760736A (en) * | 1971-10-18 | 1973-09-25 | Us Army | Non-metallic rotary bands |
| DE2758692A1 (de) * | 1977-12-29 | 1979-07-05 | Diehl Gmbh & Co | Fuehrungsband |
| US4366015A (en) * | 1980-05-16 | 1982-12-28 | Murray Myles N | Rubber driving band, artillery shell employing same, and method of making the band and assembling same in the shell |
-
1999
- 1999-12-20 EP EP99811177A patent/EP1111329A1/de not_active Withdrawn
-
2000
- 2000-12-18 EP EP00979324A patent/EP1240474B1/de not_active Expired - Lifetime
- 2000-12-18 AU AU16865/01A patent/AU1686501A/en not_active Abandoned
- 2000-12-18 WO PCT/CH2000/000669 patent/WO2001046640A1/de not_active Ceased
- 2000-12-18 DE DE50003951T patent/DE50003951D1/de not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR102960603B1 (ko) * | 2025-03-05 | 2026-04-30 | 김준규 | 무게중심이 전방에 위치한 탄두체 및 안정화된 탄도 특성을 위한 가이드링 구조를 이용한 탄도 안정화 방법 및 장치. |
Also Published As
| Publication number | Publication date |
|---|---|
| DE50003951D1 (de) | 2003-11-06 |
| AU1686501A (en) | 2001-07-03 |
| EP1111329A1 (de) | 2001-06-27 |
| EP1240474A1 (de) | 2002-09-18 |
| WO2001046640A1 (de) | 2001-06-28 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1338859B1 (de) | Waffenrohr mit Mündungsbremse | |
| DE1189890B (de) | Manoeverpatronen-Zerfallgeschoss | |
| DE10157752B4 (de) | Düsenverlängerung | |
| WO2014000805A1 (de) | Schalldämpfer für eine handfeuerwaffe | |
| DE3232825A1 (de) | Geschoss fuer handfeuerwaffen und gewehre sowie mit einem solchen geschoss versehene patrone | |
| DE2519492A1 (de) | Flexible, rohrfoermige struktur zur weiterleitung eines fluids und verfahren zu dessen herstellung | |
| EP0190548B1 (de) | Unterkalibriges Wuchtgeschoss | |
| DE3031722C2 (de) | ||
| CH660914A5 (de) | Kuehleinrichtung fuer waffenrohre von feuerwaffen. | |
| EP1111329A1 (de) | Geschoss und Verfahren zur Fertigung eines Geschosses | |
| EP0137106B1 (de) | Mantel für Treibkäfiggeschosse | |
| WO2017001428A1 (de) | AUS EINEM GEZOGENEN WAFFENROHR VERSCHIEßBARES, FLÜGELSTABILISIERTES UNTERKALIBERGESCHOSS UND VERFAHREN ZU SEINER HERSTELLUNG | |
| DE2758692A1 (de) | Fuehrungsband | |
| DE3419110A1 (de) | Geschoss mit aufgesetzter haube | |
| DE2310361A1 (de) | Plastikpfropfen fuer schrotpatronen | |
| DE10354011A1 (de) | Hülsenboden für großkalibrige Munition und Verfahren zu seiner Herstellung | |
| DE102013006498A1 (de) | Treibkäfiggeschoss | |
| EP0254019B1 (de) | Adaptionspatrone für Einsteckrohrsysteme | |
| DE3310162C2 (de) | ||
| DE1136613B (de) | Zusammengesetzter Schusswaffenlauf | |
| DE102011113539B4 (de) | Thermalisolation für Raketentriebwerke | |
| EP1111327A1 (de) | Geschoss mit einem Geschosskörper und Verfahren zur Herstellung von radial abstehenden Führungsmitteln auf einem Geschosskörper | |
| DE102009009776A1 (de) | Patrone | |
| DE19959047A1 (de) | Waffenrohr und Verfahren zur Herstellung von Waffenrohren | |
| DE2306160A1 (de) | Waelzlager-anordnung mit einem druckbelasteten beilagering und verfahren zur herstellung des beilageringes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20020701 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: RUAG COMPONENTS |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE FR LI |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: PPS POLYVALENT PATENT SERVICE AG |
|
| REF | Corresponds to: |
Ref document number: 50003951 Country of ref document: DE Date of ref document: 20031106 Kind code of ref document: P |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20031001 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040702 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20081211 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20081230 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20090223 Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20100831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091231 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091231 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100701 |