EP1208252B1 - Polytrimethylenterephthalat-stapelfasern und verfahren zu ihrer herstellung - Google Patents
Polytrimethylenterephthalat-stapelfasern und verfahren zu ihrer herstellung Download PDFInfo
- Publication number
- EP1208252B1 EP1208252B1 EP00956217A EP00956217A EP1208252B1 EP 1208252 B1 EP1208252 B1 EP 1208252B1 EP 00956217 A EP00956217 A EP 00956217A EP 00956217 A EP00956217 A EP 00956217A EP 1208252 B1 EP1208252 B1 EP 1208252B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- ptt
- melt
- spinning
- range
- sec
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 20
- 229920002215 polytrimethylene terephthalate Polymers 0.000 title description 36
- -1 polytrimethylene terephthalate Polymers 0.000 title description 2
- 239000000835 fiber Substances 0.000 claims abstract description 43
- 238000009987 spinning Methods 0.000 claims abstract description 39
- 238000000034 method Methods 0.000 claims abstract description 21
- 230000008569 process Effects 0.000 claims abstract description 18
- 229920000642 polymer Polymers 0.000 claims abstract description 11
- 238000002788 crimping Methods 0.000 claims abstract description 4
- 239000000155 melt Substances 0.000 claims description 18
- 238000001816 cooling Methods 0.000 claims description 12
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 9
- 238000010438 heat treatment Methods 0.000 claims description 8
- 229910001868 water Inorganic materials 0.000 claims description 8
- 238000007664 blowing Methods 0.000 claims description 6
- 238000002844 melting Methods 0.000 claims description 6
- 230000008018 melting Effects 0.000 claims description 6
- 230000008859 change Effects 0.000 claims description 5
- 239000000975 dye Substances 0.000 claims description 4
- 239000000203 mixture Substances 0.000 claims description 4
- 239000000986 disperse dye Substances 0.000 claims description 3
- 238000002156 mixing Methods 0.000 claims description 3
- 230000003068 static effect Effects 0.000 claims description 3
- 238000009826 distribution Methods 0.000 claims description 2
- 230000009183 running Effects 0.000 claims description 2
- 238000012546 transfer Methods 0.000 claims description 2
- 238000010521 absorption reaction Methods 0.000 claims 1
- 230000009477 glass transition Effects 0.000 claims 1
- 239000004753 textile Substances 0.000 abstract description 8
- 238000009998 heat setting Methods 0.000 abstract description 3
- 238000002074 melt spinning Methods 0.000 abstract description 3
- 238000001035 drying Methods 0.000 abstract description 2
- 238000012681 fiber drawing Methods 0.000 abstract 1
- 235000019476 oil-water mixture Nutrition 0.000 description 4
- RFFLAFLAYFXFSW-UHFFFAOYSA-N 1,2-dichlorobenzene Chemical compound ClC1=CC=CC=C1Cl RFFLAFLAYFXFSW-UHFFFAOYSA-N 0.000 description 3
- LYCAIKOWRPUZTN-UHFFFAOYSA-N Ethylene glycol Chemical compound OCCO LYCAIKOWRPUZTN-UHFFFAOYSA-N 0.000 description 3
- 239000000654 additive Substances 0.000 description 3
- MTHSVFCYNBDYFN-UHFFFAOYSA-N diethylene glycol Chemical compound OCCOCCO MTHSVFCYNBDYFN-UHFFFAOYSA-N 0.000 description 3
- 239000011521 glass Substances 0.000 description 3
- 238000012384 transportation and delivery Methods 0.000 description 3
- WERYXYBDKMZEQL-UHFFFAOYSA-N butane-1,4-diol Chemical compound OCCCCO WERYXYBDKMZEQL-UHFFFAOYSA-N 0.000 description 2
- 238000004040 coloring Methods 0.000 description 2
- QQVIHTHCMHWDBS-UHFFFAOYSA-N isophthalic acid Chemical compound OC(=O)C1=CC=CC(C(O)=O)=C1 QQVIHTHCMHWDBS-UHFFFAOYSA-N 0.000 description 2
- 238000012545 processing Methods 0.000 description 2
- 238000011282 treatment Methods 0.000 description 2
- DNIAPMSPPWPWGF-VKHMYHEASA-N (+)-propylene glycol Chemical compound C[C@H](O)CO DNIAPMSPPWPWGF-VKHMYHEASA-N 0.000 description 1
- YPFDHNVEDLHUCE-UHFFFAOYSA-N 1,3-propanediol Substances OCCCO YPFDHNVEDLHUCE-UHFFFAOYSA-N 0.000 description 1
- NMYFVWYGKGVPIW-UHFFFAOYSA-N 3,7-dioxabicyclo[7.2.2]trideca-1(11),9,12-triene-2,8-dione Chemical group O=C1OCCCOC(=O)C2=CC=C1C=C2 NMYFVWYGKGVPIW-UHFFFAOYSA-N 0.000 description 1
- 206010013786 Dry skin Diseases 0.000 description 1
- ISWSIDIOOBJBQZ-UHFFFAOYSA-N Phenol Chemical compound OC1=CC=CC=C1 ISWSIDIOOBJBQZ-UHFFFAOYSA-N 0.000 description 1
- 235000014676 Phragmites communis Nutrition 0.000 description 1
- YIMQCDZDWXUDCA-UHFFFAOYSA-N [4-(hydroxymethyl)cyclohexyl]methanol Chemical compound OCC1CCC(CO)CC1 YIMQCDZDWXUDCA-UHFFFAOYSA-N 0.000 description 1
- 239000002216 antistatic agent Substances 0.000 description 1
- 239000006085 branching agent Substances 0.000 description 1
- 239000004567 concrete Substances 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 238000013016 damping Methods 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000004043 dyeing Methods 0.000 description 1
- 230000007613 environmental effect Effects 0.000 description 1
- 125000001033 ether group Chemical group 0.000 description 1
- 238000011156 evaluation Methods 0.000 description 1
- 239000008187 granular material Substances 0.000 description 1
- 229920001519 homopolymer Polymers 0.000 description 1
- 230000001965 increasing effect Effects 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 239000000314 lubricant Substances 0.000 description 1
- 239000006224 matting agent Substances 0.000 description 1
- 238000005259 measurement Methods 0.000 description 1
- 210000003632 microfilament Anatomy 0.000 description 1
- RXOHFPCZGPKIRD-UHFFFAOYSA-N naphthalene-2,6-dicarboxylic acid Chemical compound C1=C(C(O)=O)C=CC2=CC(C(=O)O)=CC=C21 RXOHFPCZGPKIRD-UHFFFAOYSA-N 0.000 description 1
- 235000019198 oils Nutrition 0.000 description 1
- 238000012856 packing Methods 0.000 description 1
- 230000036961 partial effect Effects 0.000 description 1
- 238000006068 polycondensation reaction Methods 0.000 description 1
- 229920000728 polyester Polymers 0.000 description 1
- 229920000139 polyethylene terephthalate Polymers 0.000 description 1
- 239000005020 polyethylene terephthalate Substances 0.000 description 1
- 229920000166 polytrimethylene carbonate Polymers 0.000 description 1
- 238000012805 post-processing Methods 0.000 description 1
- 230000036316 preload Effects 0.000 description 1
- 238000011084 recovery Methods 0.000 description 1
- 230000002040 relaxant effect Effects 0.000 description 1
- 238000005507 spraying Methods 0.000 description 1
- 239000003381 stabilizer Substances 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 229920002994 synthetic fiber Polymers 0.000 description 1
- 239000012209 synthetic fiber Substances 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
Classifications
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01F—CHEMICAL FEATURES IN THE MANUFACTURE OF ARTIFICIAL FILAMENTS, THREADS, FIBRES, BRISTLES OR RIBBONS; APPARATUS SPECIALLY ADAPTED FOR THE MANUFACTURE OF CARBON FILAMENTS
- D01F6/00—Monocomponent artificial filaments or the like of synthetic polymers; Manufacture thereof
- D01F6/58—Monocomponent artificial filaments or the like of synthetic polymers; Manufacture thereof from homopolycondensation products
- D01F6/62—Monocomponent artificial filaments or the like of synthetic polymers; Manufacture thereof from homopolycondensation products from polyesters
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/29—Coated or structually defined flake, particle, cell, strand, strand portion, rod, filament, macroscopic fiber or mass thereof
- Y10T428/2913—Rod, strand, filament or fiber
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/29—Coated or structually defined flake, particle, cell, strand, strand portion, rod, filament, macroscopic fiber or mass thereof
- Y10T428/2913—Rod, strand, filament or fiber
- Y10T428/2933—Coated or with bond, impregnation or core
- Y10T428/2964—Artificial fiber or filament
- Y10T428/2967—Synthetic resin or polymer
- Y10T428/2969—Polyamide, polyimide or polyester
Definitions
- the present invention relates to PTT staple fibers [wherein PTT is equal to poly (trimethylene terephthalate)] and a process their manufacture by a two-stage spinning and stretching process.
- Staple fibers made of polyethylene terephthalate and melt spinning lines too their manufacture is known (Fourné, synthetic fibers, Hanser Verlag [1995] pages 460 - 462). Because of the different These processes are not so easy to crystallize transferable to PTT.
- EP 0 547 553 A1 describes the production of monofilaments 20 m / min spinning speed and a production speed of 100 m / min.
- EP 0 754 790 A2 describes the production of textile filaments u. a. made of PTT by means of heating surfaces heated to high temperatures as stretching aids. Concrete embodiments are missing.
- WO 99/11845 A1 describes fibers made from PTT, with birefringence of at least 0.030 is obtained.
- the specified characteristics show low elongation at break of ⁇ 90%, suitable for further processing not allow a sufficiently high draw ratio to staple fibers and are unsuitable.
- WO 99-27168 A1 discloses a high-speed spin-stretching process for the production of PTT filaments that are wound on yarn packages. Leave high throughputs and cable storage for the production of staple fibers do not derive from it.
- CA 86: 122865 for JP 52-08123 A describes the use of one per se desired high draw of 300% in the production of PTT fibers.
- the spinning speed of 360 m / min practiced for this is however so low that the economy of the process in Question is asked.
- CA 86: 122856 to JP52-05320 A describes the spinning of PTT, whereby the stretching ratio practiced to uneconomically low Spinning speeds indicates.
- the object of the present invention is to produce PTT staple fibers To provide, these and those made from them Textiles and home textiles, especially carpets, compared to conventional fibers a high degree of aesthetics and quality of use as well as environmentally friendly coloring properties.
- the Manufacturing these PTT staple fibers should be done in a two step process melt spinning and drawing, which is a higher Has economy than the previously mentioned methods for Continuous filaments.
- this object is achieved by means of PTT staple fibers and a method for producing PTT staple fibers with an intrinsic viscosity of at least 0.70 dl / g according to the Disclosure of claims.
- PTT here is a polyester with at least 90 mol% Understand trimethylene terephthalate units. Suitable as comonomers isophthalic acid, 2,6-naphthalenedicarboxylic acid, ethylene glycol, Diethylene glycol, 1,4-butanediol, 1,4-cyclohexanedimethanol. Prefers is poly (trimethylene terephthalate) homopolymer and is particularly preferred those with a low proportion of during the manufacturing process formed ether groups derived from 1,3-propanediol.
- the intrinsic The viscosity of the PTT staple fibers is in the range from 0.7 to 1.3 dl / g and particularly preferably 0.75 to 1.15 dl / g.
- the starting point is PTT melt, which either directly Polycondensation reactor is removed from the PTT production or is obtained by melting PTT granules.
- the polymer melt can contain common additives such as dyes, matting agents, Stabilizers, antistatic agents, lubricants, branching agents, in quantities contain a total of 0 to 5.0 wt .-% or the additives be added to the melt on its way to the spinnerets. Additives that contain structural characteristics (e.g. Noticeably influence the elongation at break of the filament.
- Three SMXL mixers from Sulzer / Switzerland were installed in the product line, the shear rate in the mixers being 28 sec -1 at a polymer throughput of 2500 g / min.
- the line diameter was chosen so that the shear rate in the free line was 7.9 sec -1 .
- the average residence time in the product line was about 3 minutes.
- the PTT melt was spun in a BN 100 spinning system from Lurgi Zimmer AG with a ring nozzle and radial cooling shaft.
- the hole density of the spinneret plate was 6.3 holes / cm 2 .
- the spinning beam temperature was 256 ° C., the total pressure loss of the melt until it emerged from the spinneret was 140 bar. Heat exchangers were not installed.
- the residence time in the nozzle pack was approximately 0.5 min.
- the melt filaments emerging from the nozzle plate were cooled in an amount of 1400 Nm 3 / h and at a temperature of 8 ° C. by means of cooling air guided radially inwards from the outside.
- the solidified spun threads were placed at a distance of 850 mm from the underside of the nozzle plate on a ring oiler and a water-oil mixture was applied so that the amount of water on the spun threads was about 25% by weight and a very stable thread run resulted ,
- the spinning take-off speed was 900 m / min. After the stripping, the spinning threads were deposited in spinning cans in the form of spinning cables by means of a reel mill.
- the separate stretching of the spinning cable was carried out in a fiber section in two stages.
- the spinning cables were then heat-set at slight relaxation, cooled, crimped, dried and closed Cut staple fibers.
- the production speed in the Fiber section, according to the speed of the roller mill on Outflow from the last stretching zone was 100 m / min.
- the intrinsic viscosities were determined on a solution of 0.5 g PTT in 100 ml of a mixture of phenol and 1,2-dichlorobenzene (3: 2 parts by weight) measured at 25 ° C.
- Melting point and glass point were determined by means of DSC at a heating rate of 10 ° C / min after the sample has been melted briefly and was immediately deterred.
- the titer and force-elongation properties of the fibers were compared with the Device set, Vibrotex and Vibrodyn, from Lenzing / Austria determined.
- the clamping length was 20 mm, depending on the preload weight of titer 100 mg / dtex and the test speed 20 mm / min.
- the LASE values (load at specific elongation) could be entered by entering the Reference stretches can be taken directly from the evaluation device.
- the Secant module was created by applying a secant to the elongation value (Elongation at break minus 45%), however at least 5%, and the Slope of this straight line in (cN / tex) with respect to 1% elongation change evaluated.
- the hot air shrink was in the heating cabinet at one Temperature treatment of 180 ° C over a dwell time of 20 min without Bias of the fiber determined.
- the crimp sheets were counted visually.
- the crimp values were determined according to the method and with the Vibrotex device from Lenzing / AT.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Artificial Filaments (AREA)
- Spinning Methods And Devices For Manufacturing Artificial Fibers (AREA)
- Yarns And Mechanical Finishing Of Yarns Or Ropes (AREA)
- Polyesters Or Polycarbonates (AREA)
Description

| Beispiel Nr. | 1 | 2 | |
| PTT-Schmelzpunkt Tm | °C | 227 | 227 |
| PTT-Glaspunkt | °C | 46 | 46 |
| PTT - I.V. | dl/g | 0,93 | 0,93 |
| Schmelzetemperatur Ts | °C | 255 | 255 |
| Leitungstemperatur TL | °C | 255 | 255 |
| Scherrate Leitung | sec-1 | 7,9 | 7,9 |
| Scherrate Mischer | sec-1 | 28 | 28 |
| Temperaturänderung im Wärmetauscher | dTw °C | 0 | 0 |
| Gesamtdruckverlust | dp(bar) | 140 | 175 |
| Spinnbalkentemperatur | °C | 256 | 256 |
| Lochdichte Düsenplatte | n/cm2 | 6,3 | 1 |
| Fördermenge pro Düsenloch | g/min | 0,668 | 4,15 |
| Spinnverzug | 1: | 77 | 12 |
| Anblaslänge | mm | 200 | 300 |
| Kühlluft-Temperatur | °C | 8 | 8 |
| Kühlluft-Menge | Nm3/h | 1400 | 1500 |
| mittlere Kühlluft-Geschwindigkeit | m/sec | 1,5 | 1,1 |
| Spinnpräparationskonzentration | % | 0,5 | 0,5 |
| Abzugsgeschwindigkeit | m/min | 900 | 800 |
| Faserstrecke-Einlaufgeschwindigkeit | m/min | 32,8 | 19,2 |
| 1. Streckzone-Temperatur | °C | 57 | 57 |
| Streckzone-Verstreckverh. | 1: | 2,7 | 3,4 |
| 2. Streckzone-Temperatur | °C | 70 | 80 |
| Streckzone-Verstreckverh. | 1: | 1,13 | 1,15 |
| Fixierzone-Temperatur | °C | 90 | 100 |
| Fixierzone-Relaxbetrag | 1: | 0,94 | 1,00 |
| Auslaufgeschw.-Relaxzone | m/min | 94 | 75 |
| Trockner-Temperatur | °C | 70 | 150 |
| Trockner-Verweilzeit | min | 2,5 | 2,5 |
| Gesamtverstreckverhältnis | 1: | 3,05 | 3.91 |
| Tatsächlicher Relaxbetrag der Faser | 1: | 0,90 | 0,74 |
| Spinnfäden | |||
| - Titer | dtex | 7,87 | 50,6 |
| - Reißfestigkeit | cN/tex | 13,9 | 10,7 |
| - Reißdehnung | % | 314 | 613 |
| - I.V. | dl/g | 0,90 | 0,90 |
| - Dichte | g/cm3 | 1,3207 | 1,3178 |
| Stapelfasern | |||
| - Titer | dtex | 3,05 | 17,2 |
| - CV-Titer | % | 5 | 5,3 |
| - Reißfestigkeit | cN/dtex | 35,8 | 28,0 |
| - Reißdehnung | % | 54,9 | 72,4 |
| - CV-Reißdehnung | % | 9,2 . | 12,1 |
| - LASE (2 %) | cN/tex | 3 | 2,5 |
| - LASE (5 %) | cN/tex | 6 | 5 |
| - LASE (10 %) | cN/tex | 7,9 | 7,2 |
| - Sekantenmodul (Rd-45 %) | cN/tex pro 1 % | 0,5 | 0,32 |
| - Anzahl Kräuselbögen | n/cm | 11 | 13 |
| - Kräuselwert | % | 12 | 13 |
| - Kräuselbeständigkeit | % | 86 | 81 |
| - Heißluftschrumpf | % | 16 | 3 |
| - Schnittlänge | mm | 38 | 150 |
Claims (8)
- PTT-Stapelfasern, dadurch gekennzeichnet, daß sie eine Intrinsic Viskosität im Bereich von 0,70 - 1,3 dl/g, einen LASE (10 %) von 5 bis 12 cN/tex, einen Sekantenmodul (Rd-45 %) von < 1,0 cN/tex pro 1 %, eine Kräuselbeständigkeit von > 75 % aufweisen und ohne Zusatz von Carrier/Farbstoffaufziehhilfen mit Dispersionsfarbstoffen anfärbbar sind.
- PTT-Stapelfasern gemäß Anspruch 1, dadurch gekennzeichnet, daß sie eine Intrinsic Viskosität im Bereich von 0,75 bis 1,15 dl/g und einen Titer im Bereich von 0,8 bis 20 den aufweisen.
- Verfahren zur Herstellung von PTT-Stapelfasern mit einer Intrinsic Viskosität von mindestens 0,70 dl/g durch einen zweistufigen Spinn- und Streckprozeß, dadurch gekennzeichnet, daßwobei die Produktionsgeschwindigkeit 25 bis 400 m/min beträgt, anschließend unter die Glasumwandlungstemperatur abgekühlt werden und nach Zusammenlegen zu mindestens einem Kabel in je einer Strauchkammerkräuselmaschine pro Kabel gekräuselt werden, die Kabel wahlweise mmit einer Öl-Wasser-Mischung nachpräpariert und danach bei 30 bis 200 °C innerhalb von 0,5 bis 10 min getrocknet und schließlich in einem direkt anschließenden oder separatem Arbeitsgang zu Stapelfasern geschnitten werden.a) eine PTT-Schmelze mit einer Temperatur Ts (°C) = TM + k, wobei TM die Schmelztemperatur des PTT und 7 ≤ k ≤ 63 ist, durch eine mittels eines externen Wärmeträgermediums mit einer Temperatur TL im Bereich von 234 bis 290 °C beheizte Produktleitung einem auf TB 234 bis 290°C beheizten Spinnbalken mit in Strömungsrichtung mindestens je einer(m) Spinnpumpe, Spinndüsenpaket und Düsenplatte mit einer Lochdichte von 0,3 bis 20 Loch/cm2 zugeführt und durch die mindestens eine Düsenplatte zu Schmelzefäden versponnen wird, wobei die mittlere Verweilzeit der PTT-Schmelze in der Produktleitung weniger als 30 min und im Spinndüsenpaket maximal 4 min und der Spinnverzug 1 : 30 bis 1 : 160 beträgt, und die Fördermenge F in g/min pro Düsenloch bezogen auf den Fasertiter in dtex im Bereich 0,14 bis 0,66 liegt,b) die Schmelzefäden mit senkrecht zur Fadenlaufrichtung einströmender, turbulenzfreier Kühlluft von 5 bis 25 °C bei einer mittleren Luftaüstrittsgeschwindigkeit von 0,5 bis 2,0 m/sec und einer Anblaszonenlänge von 50 bis 2000 mm abgekühlt werden, und die abgekühlten Fäden mit einer Wasser-Öl-Mischung so beaufschlagt werden, daß 12 bis 30 Gew.-% Wasser auf den Fäden verbleiben, und die Fäden zu Filamentbündeln zusammengefaßt werden, die ihrerseits zu Spinnkabeln vereinigt werden, welche mit einer Abzugsgeschwindigkeit im Bereich von 600 bis 2000 m/min abgezogen und in Kannen abgelegt werden,c) die Spinnkabel aus den Kannen über ein Einlaufwerk und Riet abgezogen und einer Faserstrecke zugeführt werden, in der sie in mindestens einer Verstreckstufe bei 20 bis 100 °C verstreckt, wahlweise bei maximal 210 °C thermofixiert und relaxiert werden,
- Verfahren nach Anspruch 3, dadurch gekennzeichnet, daß TL = Ts ± 15 °C innerhalb des Bereiches von 234 bis 290 °C ist und die Wandscherrate der PTT-Schmelze in der Produktleitung 2 bis 128 sec-1 beträgt.
- Verfahren nach Anspruch 3 oder 4, dadurch gekennzeichnet, daß die Produktleitung in Stufe a) wahlweise mindestens je ein(e) statisches Mischelement, Boosterpumpe, Polymerfilter, Polymerwärmetauscher, Absperr- und Verteilerarmatur einschließt, und die Wandscherrate der PTT-Schmelze in der freien Produktleitung 3,5 bis 16 sec-1 und innerhalb eines statischen Mischelementes 12 bis 128 sec-1beträgt.
- Verfahren nach einem der Ansprüche 3 bis 5, dadurch gekennzeichnet, daß der Düsenlochdurchmesser D entsprechendgewählt wird, und TB(°C) = Ts + dTw + 4/100 ·dp(bar) ± 15 ist, wobei ζ die Dichte der PTT-Schmelze, dTw die Änderung der Schmelzetemperatur im Wärmetauscher, die positiv für Heizung und negativ für Kühlung angesetzt wird, und dp(bar) der Gesamtdruckverlust der Schmelze bis zum Austritt aus der Spinndüsenplatte ist.
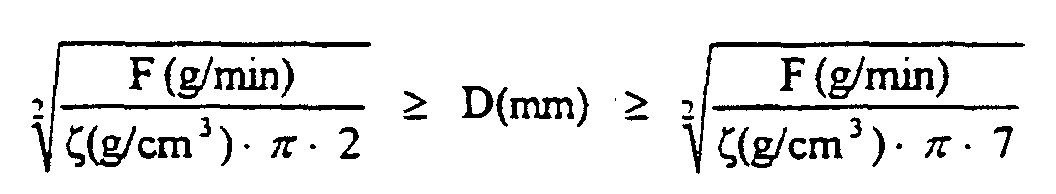
- Verfahren nach einem der Ansprüche 3 bis 6, dadurch gekennzeichnet, daß die Anblaszonenlänge 150 bis 600 mm bei Radialanblasung und 500 bis 2000 mm bei Querstromanblasung beträgt.
- Verfahren nach einem der Ansprüche 3 bis 7, dadurch gekennzeichnet, daß das Verstreckverhältnis VV entsprechend VV(%)= 1 + α · Rd/100 eingestellt wird, wobei Rd die Dehnung in % des Spinnfadens und α = 0,25 bis 0,75 ist, und die Auslaufgeschwindigkeit aus der Relaxzone mindestens 90 m/min beträgt.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19934551A DE19934551A1 (de) | 1999-07-22 | 1999-07-22 | PTT-Stapelfasern und Verfahren zu ihrer Herstellung |
| DE19934551 | 1999-07-22 | ||
| PCT/EP2000/006923 WO2001007693A1 (de) | 1999-07-22 | 2000-07-20 | Polytrimethylenterephthalat-stapelfasern und verfahren zu ihrer herstellung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1208252A1 EP1208252A1 (de) | 2002-05-29 |
| EP1208252B1 true EP1208252B1 (de) | 2004-03-24 |
Family
ID=7915781
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP00956217A Expired - Lifetime EP1208252B1 (de) | 1999-07-22 | 2000-07-20 | Polytrimethylenterephthalat-stapelfasern und verfahren zu ihrer herstellung |
Country Status (14)
| Country | Link |
|---|---|
| US (1) | US6645621B1 (de) |
| EP (1) | EP1208252B1 (de) |
| JP (1) | JP2003505614A (de) |
| KR (1) | KR100649850B1 (de) |
| CN (1) | CN1187485C (de) |
| AT (1) | ATE262602T1 (de) |
| AU (1) | AU6825100A (de) |
| CA (1) | CA2378747A1 (de) |
| DE (2) | DE19934551A1 (de) |
| EA (1) | EA003017B1 (de) |
| ES (1) | ES2218204T3 (de) |
| MX (1) | MXPA01013327A (de) |
| PL (1) | PL357349A1 (de) |
| WO (1) | WO2001007693A1 (de) |
Families Citing this family (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ATE298810T1 (de) * | 2000-03-15 | 2005-07-15 | Shell Int Research | Poly(trimethylene) terephthalate textil stapelfaserherstellung |
| US6752945B2 (en) * | 2000-09-12 | 2004-06-22 | E. I. Du Pont De Nemours And Company | Process for making poly(trimethylene terephthalate) staple fibers |
| US6458455B1 (en) | 2000-09-12 | 2002-10-01 | E. I. Du Pont De Nemours And Company | Poly(trimethylene terephthalate) tetrachannel cross-section staple fiber |
| US6539596B1 (en) | 2000-09-25 | 2003-04-01 | Shell Oil Company | Nonwovens from polytrimethylene terephthalate based staple fibers |
| DE60218207T2 (de) * | 2001-10-24 | 2007-11-22 | Teijin Ltd. | Verfahren zur herstellung von kurzfasern aus polytrimethylenterephthalat |
| US7578957B2 (en) | 2002-12-30 | 2009-08-25 | E. I. Du Pont De Nemours And Company | Process of making staple fibers |
| EP1600467A4 (de) * | 2003-03-05 | 2006-03-29 | Asahi Kasei Chemicals Corp | Poly(trimethylenterphthalat)-zusammensetzung und herstellungsverfahren dafür |
| US20050147784A1 (en) * | 2004-01-06 | 2005-07-07 | Chang Jing C. | Process for preparing poly(trimethylene terephthalate) fiber |
| US8021736B2 (en) * | 2006-07-13 | 2011-09-20 | E.I. Du Pont De Nemours And Company | Substantially flame retardant-free 3GT carpet |
| US20090036613A1 (en) | 2006-11-28 | 2009-02-05 | Kulkarni Sanjay Tammaji | Polyester staple fiber (PSF) /filament yarn (POY and PFY) for textile applications |
| KR101039052B1 (ko) * | 2008-08-05 | 2011-06-07 | 코리아나까조 주식회사 | 제빙기의 정수위조절장치 |
| KR101037197B1 (ko) * | 2008-08-05 | 2011-05-26 | 코리아나까조 주식회사 | 제빙장치 |
| KR101044732B1 (ko) * | 2009-01-30 | 2011-06-28 | 웅진케미칼 주식회사 | 부직포용 단섬유 및 그의 제조방법 |
| CN110699766A (zh) * | 2019-11-13 | 2020-01-17 | 江苏理工学院 | 一种纺丝侧吹风均风装置 |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS4921256B1 (de) | 1969-03-12 | 1974-05-30 | ||
| US4159617A (en) | 1969-11-17 | 1979-07-03 | Fiber Industries, Inc. | Resilient polyester fibers |
| US5234764A (en) * | 1988-07-05 | 1993-08-10 | Allied-Signal Inc. | Dimensionally stable polyester yarn for high tenacity treaty cords |
| MX9603276A (es) | 1994-02-21 | 1997-03-29 | Degussa | Un proceso para colorear fibras de tereftalato politrimetileno y el uso de las fibras coloreadas por este proceso. |
| JPH11189938A (ja) * | 1997-12-24 | 1999-07-13 | Toray Ind Inc | ポリプロピレンテレフタレート短繊維およびその製造方法 |
| DE19937727A1 (de) * | 1999-08-10 | 2001-02-15 | Lurgi Zimmer Ag | Polyester-Stapelfasern und Verfahren zu deren Herstellung |
-
1999
- 1999-07-22 DE DE19934551A patent/DE19934551A1/de not_active Withdrawn
-
2000
- 2000-07-20 CA CA002378747A patent/CA2378747A1/en not_active Abandoned
- 2000-07-20 US US10/031,467 patent/US6645621B1/en not_active Expired - Fee Related
- 2000-07-20 PL PL00357349A patent/PL357349A1/xx unknown
- 2000-07-20 CN CNB008106274A patent/CN1187485C/zh not_active Expired - Fee Related
- 2000-07-20 JP JP2001512957A patent/JP2003505614A/ja active Pending
- 2000-07-20 EA EA200200099A patent/EA003017B1/ru not_active IP Right Cessation
- 2000-07-20 WO PCT/EP2000/006923 patent/WO2001007693A1/de not_active Ceased
- 2000-07-20 MX MXPA01013327A patent/MXPA01013327A/es active IP Right Grant
- 2000-07-20 ES ES00956217T patent/ES2218204T3/es not_active Expired - Lifetime
- 2000-07-20 KR KR1020027000821A patent/KR100649850B1/ko not_active Expired - Fee Related
- 2000-07-20 DE DE50005808T patent/DE50005808D1/de not_active Expired - Fee Related
- 2000-07-20 AT AT00956217T patent/ATE262602T1/de not_active IP Right Cessation
- 2000-07-20 AU AU68251/00A patent/AU6825100A/en not_active Abandoned
- 2000-07-20 EP EP00956217A patent/EP1208252B1/de not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| EA200200099A1 (ru) | 2002-04-25 |
| US6645621B1 (en) | 2003-11-11 |
| DE19934551A1 (de) | 2001-01-25 |
| EP1208252A1 (de) | 2002-05-29 |
| CA2378747A1 (en) | 2001-02-01 |
| ATE262602T1 (de) | 2004-04-15 |
| CN1369026A (zh) | 2002-09-11 |
| JP2003505614A (ja) | 2003-02-12 |
| WO2001007693A1 (de) | 2001-02-01 |
| MXPA01013327A (es) | 2004-03-10 |
| KR20020015075A (ko) | 2002-02-27 |
| KR100649850B1 (ko) | 2006-11-24 |
| ES2218204T3 (es) | 2004-11-16 |
| EA003017B1 (ru) | 2002-12-26 |
| DE50005808D1 (de) | 2004-04-29 |
| PL357349A1 (en) | 2004-07-26 |
| CN1187485C (zh) | 2005-02-02 |
| AU6825100A (en) | 2001-02-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE10022889B4 (de) | Verfahren zum Herstellen von synthetischen Fäden aus einer Polymermischung auf Polyesterbasis | |
| EP1002146B1 (de) | Verfahren zur verarbeitung von polymermischungen zu filamenten | |
| DE60114954T2 (de) | Polytrimethylenterephthalatgarn | |
| DE2117659A1 (de) | Verfahren zum Herstellen von Fäden und Fasern | |
| DE69608565T2 (de) | Polyesterkabel | |
| DE69221739T2 (de) | Herstellung von feinen polyesterfilamenten | |
| EP1208252A1 (de) | Polytrimethylenterephthalat-stapelfasern und verfahren zu ihrer herstellung | |
| EP1208255B1 (de) | Hochfeste polyesterfäden und verfahren zu deren herstellung | |
| DE69420747T2 (de) | Endlosfilamente, faden und kabel | |
| DE19707447A1 (de) | Verfahren zur Verarbeitung von Polymermischungen zu Filamenten | |
| US5993712A (en) | Process for the processing of polymer mixtures into filaments | |
| EP1356143B1 (de) | Verfahren zum spinnen und aufspulen von pet-filamenten | |
| EP0630995B1 (de) | Multifilament-Garn aus Polyäthylennaphthalat und Verfahren zu seiner Herstellung | |
| DE69319159T2 (de) | Garn-Streckverfahren unter Anwendung von Dampf | |
| DE69126914T2 (de) | Verfahren zum Spinnen von synthetischen Fasern mit hoher Festigkeit, hohem Modul und niedrigem Schrumpf | |
| DE69323808T2 (de) | Verfahren für das Hochdruckspinnen von Polyester-Industriegarn | |
| EP1330563B1 (de) | Verfahren zum spinnen und aufspulen von polyester-filamenten, durch das spinn-verfahren erhältliche polyester-filamente, strecktexturierung der polyester-filamente sowie durch die strecktexturierung erhältliche bauschige polyester-filamente | |
| EP1334223B1 (de) | Verfahren zum herstellen von synthetischen fäden aus polymermischungen | |
| EP1208253B1 (de) | Hmls-fäden aus polyester und spinnstreckverfahren zu deren herstellung | |
| DE10338821B4 (de) | Verfahren zur Herstellung von feinen Fasern | |
| DE19747867B4 (de) | Verfahren zur Herstellung von Filamenten aus Polymermischungen | |
| DE68902927T2 (de) | Verfahren fuer dimensionell stabiles polyestergarn. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20020222 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RTI1 | Title (correction) |
Free format text: DISCONTINUOUS POLYTRIMETHYLENE TEREPHTHALATE FIBRES AND METHOD FOR PRODUCING THE SAME |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040324 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040324 Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040324 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040324 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040324 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50005808 Country of ref document: DE Date of ref document: 20040429 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040624 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040624 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040720 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040720 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040731 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040731 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20040324 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20040324 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2218204 Country of ref document: ES Kind code of ref document: T3 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| BERE | Be: lapsed |
Owner name: *ZIMMER A.G. Effective date: 20040731 |
|
| 26N | No opposition filed |
Effective date: 20041228 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20070719 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20070727 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD Ref country code: FR Ref legal event code: CA |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20070713 Year of fee payment: 8 |
|
| BERE | Be: lapsed |
Owner name: *ZIMMER A.G. Effective date: 20040731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040824 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20070725 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20070710 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090203 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20090331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080731 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080720 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080731 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20080721 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080721 |