EP1105237B1 - Verfahren zur prozessüberwachung beim druckgiessen oder thixoformen von metallen - Google Patents
Verfahren zur prozessüberwachung beim druckgiessen oder thixoformen von metallen Download PDFInfo
- Publication number
- EP1105237B1 EP1105237B1 EP99944412A EP99944412A EP1105237B1 EP 1105237 B1 EP1105237 B1 EP 1105237B1 EP 99944412 A EP99944412 A EP 99944412A EP 99944412 A EP99944412 A EP 99944412A EP 1105237 B1 EP1105237 B1 EP 1105237B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- calculated
- time
- temperature
- variation
- solidification
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 31
- 238000004512 die casting Methods 0.000 title claims abstract description 19
- 238000012544 monitoring process Methods 0.000 title claims abstract description 17
- 229910052751 metal Inorganic materials 0.000 title claims abstract description 14
- 239000002184 metal Substances 0.000 title claims abstract description 14
- 150000002739 metals Chemical class 0.000 title claims abstract description 4
- 238000007711 solidification Methods 0.000 claims abstract description 37
- 230000008023 solidification Effects 0.000 claims abstract description 37
- 230000001960 triggered effect Effects 0.000 claims description 5
- 238000007493 shaping process Methods 0.000 claims description 3
- 238000004519 manufacturing process Methods 0.000 description 8
- 229910045601 alloy Inorganic materials 0.000 description 4
- 239000000956 alloy Substances 0.000 description 4
- 238000001816 cooling Methods 0.000 description 4
- 230000002123 temporal effect Effects 0.000 description 4
- 229910000838 Al alloy Inorganic materials 0.000 description 3
- 238000009423 ventilation Methods 0.000 description 3
- 238000009529 body temperature measurement Methods 0.000 description 2
- 229910001338 liquidmetal Inorganic materials 0.000 description 2
- 239000000523 sample Substances 0.000 description 2
- 238000012360 testing method Methods 0.000 description 2
- 238000012546 transfer Methods 0.000 description 2
- 229910000861 Mg alloy Inorganic materials 0.000 description 1
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 1
- 238000009530 blood pressure measurement Methods 0.000 description 1
- 238000005266 casting Methods 0.000 description 1
- 238000012937 correction Methods 0.000 description 1
- 238000001514 detection method Methods 0.000 description 1
- 239000000314 lubricant Substances 0.000 description 1
- 238000005259 measurement Methods 0.000 description 1
- 239000000155 melt Substances 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D17/00—Pressure die casting or injection die casting, i.e. casting in which the metal is forced into a mould under high pressure
- B22D17/007—Semi-solid pressure die casting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D17/00—Pressure die casting or injection die casting, i.e. casting in which the metal is forced into a mould under high pressure
- B22D17/20—Accessories: Details
- B22D17/32—Controlling equipment
Definitions
- the invention relates to a method for process monitoring in die casting or thixoforms of metals in a vacuum in a mold.
- the invention has for its object a method of the aforementioned To create the way with which the production of die-cast and thixoform parts continuously and reliably monitored under production conditions can be.
- the temporal course leads to the achievement of the object according to the invention the temperature is continuously measured at at least one point in the system and by means of a program the temperature curve of the system in Real time is calculated, and that from the temperature curve of the system the temporal course of the heat flow and from the heat flow the temporal Course of the energy of the system and the amount of heat of solidification of the in the shape of solidified metal is calculated, at a specified time calculated values can be used as characteristic values for monitoring.
- the amount of heat per unit time between the metal to be cast and exchanging the mold halves determines the rate of solidification of the part produced by die casting or thixoforming. Since the Characteristics of this exchange directly the mechanical properties of the die-cast or thixiform part is the monitoring of Solidification of the metal in the form to maintain a high quality standard essential.
- the detection of the amount of solidification heat dissipated via the mold enables it u.a. determine whether the solidification is completely within the shape takes place whether pre-solidification occurs or what liquid-solid ratio is present in a thixomaterial.
- the amount of latent heat depends on the liquid metal content Filling the mold cavity.
- the amount of dispensed over the mold halves latent heat in turn depends on the metal to be cast or on the alloy used and can further by the temperature of the mold or the mold halves, by the pressure exerted, by the piston speed as well as the thickness of the lubricant layer.
- the heat exchange that occurs during the various phases of solidification takes place is calculated using a program.
- the calculations lie Based on temperature measurements on the mold, preferably the temperature measured in the mold wall and the temporal course of the temperature is calculated on the shaping surface of the mold.
- the program takes into account inverse heat conduction and calculates the temperature in real time the shaping surface of the mold halves and the heat exchange between the solidifying metal and the shape. With those arranged in this way Temperature sensors can ensure the uniformity of the cooling process and the thermal equilibrium on the mold surface in the different successive phases of casting and cooling in Be monitored in real time. The sensors are therefore preferred in places arranged where the thermal equilibrium and solidification are good too are recorded.
- a characteristic value for the amount of solidification heat dissipated at a specified time is preferably between about 20% and 100%, in particular between about 50% and 100% of the maximum amount of solidification heat.
- the time course of the Heat exchange coefficients can be calculated.
- the one at a particular Time calculated value for the heat exchange coefficient e.g. the maximum values in the solidification or cooling phase, or also the entire curve, can be used as additional parameters.
- the time course of the solidification length can be derived from the time course of the temperature be calculated.
- the solidification length is that of Mold surface understood from the measured thickness of the solidified metal.
- the solidification length calculated at a specified time can be used as a further additional length Characteristic value can be used.
- the calculated or measured characteristic values can be used for process monitoring are compared as actual values with corresponding target values, whereby it can be provided that in the event of an impermissibly large deviation of the actual values an alarm is triggered by the setpoints within a tolerance range and if the tolerance range of the die casting or thixoforming process is exceeded is interrupted.
- the setpoint for the amount of solidification heat removed is, for example given as the mean with a standard deviation.
- the standard deviation can be set as the first tolerance limit, for example Exceeded by the actual value triggers an alarm.
- Deviations of the actual values from the target values are in real time recorded so that appropriate corrective action can be taken quickly can be.
- a particularly interesting field of application of the method lies in Die casting and thixoforming, in particular of aluminum and magnesium alloys, for example for the production of safety components for the Vehicle industry.
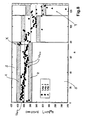
- the examination results shown in FIG. 8 show that with the monitoring method according to the invention with regard to the solidification process a high quality standard can be achieved. deviations are displayed immediately online.
- the calculated values can, for example via a RS232 interface to a programmable machine, which controls the die casting machine.
- the data are checked, if necessary displayed and finally archived. Fall the calculated Values for the amount of solidification in the tolerance range R, see above an alarm can be triggered directly by the machine. With more deviating Values that fall within the range S can, for example, be automatic Production stop can be triggered.
- Process monitoring can be carried out at various points in the mold halves Temperature sensors are arranged. The calculations are preferred carried out individually for the individual temperature sensors and also individually recorded as monitoring results. In this way it is possible to locate specific production problems on the mold. The recorded Monitoring results are conveniently archived and can later be used, for example, to prove the production quality of a particular Die-cast or thixiform part can be used.
- a die casting system 10 has a filling chamber 12 with a filling chamber cavity 14 on. That from a furnace 18 via a feed line 20 for everyone Shot in the filling chamber cavity 14 filled with liquid metal a piston 16 via a sprue 22 from the filling chamber cavity 14 in one of a fixed mold half 24 and a movable mold half 26 formed mold cavity 28 shot.
- the mold cavity 28 has one or more ventilation channels 30 which possibly combined into a collecting channel.
- a control insert 32 with a control pin 34 arranged in the fixed Mold half 24 .
- the control bolt 34 has a locking head 36 for opening or closing the ventilation channel 30.
- the shift of the Control bolt 34 is carried out by means of an actuating cylinder 38. When this is done The mold is filled via the locking head 36 of the control bolt 34 the ventilation channel 30 is closed at the end of the mold cavity 28.
- a vacuum line 40 connects to the control insert 32 Valves 42 connected to a vacuum container, not shown in the drawing is. Before the metal is shot into the mold cavity 28 this evacuates and the time course of the pressure in the mold cavity 28 over a pressure sensor 44 connected into the vacuum line 40 is measured.
- Temperature sensors are located at different points in the two mold halves 24, 26 46 arranged. Not shown in the drawing is one with the Mold cavity related probe to measure relative Humidity.
- the temperature sensors 46, the pressure sensor 44 and the one not shown Probe for measuring the relative humidity are connected to a program-controlled Computer 48 connected.
- This computer transfers the measured and calculated parameters to a data acquisition device 50 for monitoring and archiving.
- the triggering of an alarm or a production stop if tolerance values for individual or all characteristic values are exceeded takes place directly on the computer.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
- Encapsulation Of And Coatings For Semiconductor Or Solid State Devices (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
- Injection Moulding Of Plastics Or The Like (AREA)
- Continuous Casting (AREA)
- Investigating Or Analyzing Materials Using Thermal Means (AREA)
Description
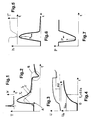
- Fig. 1 den zeitlichen Verlauf des Wärmeflusses;
- Fig. 2 den zeitlichen Temperaturverlauf während eines Druckgiesszyklus;
- Fig. 3 den zeitlichen Verlauf der Energie während eines Druckgiesszyklus;
- Fig. 4 den zeitlichen Verlauf der Erstarrungswärmemenge im Bereich A von Fig. 2;
- Fig. 5 den zeitlichen Verlauf der Temperatur bei der Abkühlung der Form im Bereich B von Fig. 2;
- Fig. 6 den zeitlichen Verlauf des Wärmeaustauschkoeffizienten bei der Abkühlung der Form im Bereich B von Fig. 2;
- Fig. 7 den zeitlichen Verlauf des Drucks im Formhohlraum;
- Fig. 8 die Erstarrungswärmemenge als Kennwert für drei verschiedene Aluminiumlegierungen bei zunehmender Schusszahl;
- Fig. 9 eine Druckgiessanlage mit Prozessüberwachung.
- t
- Zeit
- To
- berechnete Temperatur an der formgebenden Oberfläche
- T
- gemessene Temperatur in der Formwand, 1 mm unter der Oberfläche
- Tv
- Oberflächentemperatur der Form unmittelbar vor dem Schuss
- U
- Energie
- ΔU
- Energiedifferenz zwischen Beginn der Formfüllung und nach Abkühlung der Form
- UE
- Erstarrungswärmemenge
- Ue1s,i
- Soll- bzw. Istwert der Erstarrungswärmemenge bei der Zeit t1 = 0.5 s
- W
- Wärmefluss
- h
- Wärmeaustauschkoeffizient
- p
- Druck im Formhohlraum
- rH
- relative Feuchtigkeit im Formhohlraum
- n
- Schusszahl
Claims (12)
- Verfahren zur Prozessüberwachung beim Druckgiessen oder Thixoformen von Metallen im Vakuum in einer Form,
dadurch gekennzeichnet, dass
der zeitliche Verlauf der Temperatur (T) an mindestens einer Stelle des Systems kontinuierlich gemessen und mittels eines Programmes der Temperaturverlauf des Systems in Echtzeit berechnet wird, und dass aus dem Temperaturverlauf des Systems der zeitliche Verlauf des Wärmeflusses (W) und aus dem Wärmefluss der zeitliche Verlauf der Energie (U) des Systems sowie der Erstarrungswärmemenge (UE) des in der Form erstarrten Metalls berechnet wird, wobei zu einem festgelegten Zeitpunkt berechnete Werte als Kennwerte für die Überwachung verwendet werden. - Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass die Temperatur (T) in der Formwand gemessen und der zeitliche Verlauf der Temperatur (To) an der formgebenden Oberfläche der Form berechnet wird.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, dass ein Kennwert für die zu einer festgelegten Zeit (t1) abgeführte Erstarrungswärmemenge (UE1) beim Druckgiessen zwischen 20% und 100%, vorzugsweise zwischen 50% und 100% der maximalen Erstarrungswärmemenge (UEmax) liegt.
- Verfahren nach einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, dass als Kennwert beim Druckgiessen die Erstarrungswärmemenge (UE1) bei einer festgesetzten Zeit (t1) von 0.1 bis 2 s, vorzugsweise 0.3 bis 0.8 s und insbesondere etwa 0.5 s berechnet wird.
- Verfahren nach einem der Ansprüche 1 bis 4, dadurch gekennzeichnet, dass die unmittelbar vor jedem Schuss für die Formoberfläche berechnete Temperatur (Tv) als weiterer Kennwert verwendet wird.
- Verfahren nach einem der Ansprüche 1 bis 5, dadurch gekennzeichnet, dass aus dem zeitlichen Verlauf der Temperatur (T) der zeitliche Verlauf des Wärmeaustauschkoeffizienten (h) berechnet und der Wärmeaustauschkoeffizient als weiterer Kennwert verwendet wird.
- Verfahren nach einem der Ansprüche 1 bis 6, dadurch gekennzeichnet, dass aus dem zeitlichen Verlauf der Engergie (U) des Systems die Differenz (ΔU) zwischen den Energiewerten zu Beginn der Formfüllung bei aufeinanderfolgenden Schüssen als weiterer Kennwert verwendet wird.
- Verfahren nach einem der Ansprüche 1 bis 7, dadurch gekennzeichnet, dass aus dem zeitlichen Verlauf der Temperatur (T) der zeitliche Verlauf der Erstarrungslänge berechnet und die zu einer festgelegten Zeit berechnete Erstarrungslänge als weiterer Kennwert verwendet wird.
- Verfahren nach einem der Ansprüche 1 bis 8, dadurch gekennzeichnet, dass der zeitliche Verlauf des Drucks (p) in der Form gemessen und der minimale Druck (pmin) als weiterer Kennwert verwendet wird.
- Verfahren nach einem der Ansprüche 1 bis 9, dadurch gekennzeichnet, dass die minimale relative Feuchtigkeit (rH) unmittelbar vor einem Schuss in der Form gemessen und als weiterer Kennwert verwendet wird.
- Verfahren nach einem der Ansprüche 1 bis 10, dadurch gekennzeichnet, dass die berechneten oder gemessenen Kennwerte als Istwerte mit entsprechenden Sollwerten verglichen werden.
- Verfahren nach Anspruch 11, dadurch gekennzeichnet, dass bei unzulässig starker Abweichung der Istwerte von den Sollwerten innerhalb eines Toleranzbereiches ein Alarm ausgelöst und bei Überschreiten des Toleranzbereiches der Druckgiess- oder Thixoformvorgang unterbrochen wird.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP99944412A EP1105237B1 (de) | 1998-08-27 | 1999-08-16 | Verfahren zur prozessüberwachung beim druckgiessen oder thixoformen von metallen |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP98810846A EP0982089A1 (de) | 1998-08-27 | 1998-08-27 | Verfahren zur Prozessüberwachung beim Druckgiessen oder Thixoformen von Metallen |
| EP98810846 | 1998-08-27 | ||
| PCT/EP1999/006002 WO2000012246A1 (de) | 1998-08-27 | 1999-08-16 | Verfahren zur prozessüberwachung beim druckgiessen oder thixoformen von metallen |
| EP99944412A EP1105237B1 (de) | 1998-08-27 | 1999-08-16 | Verfahren zur prozessüberwachung beim druckgiessen oder thixoformen von metallen |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1105237A1 EP1105237A1 (de) | 2001-06-13 |
| EP1105237B1 true EP1105237B1 (de) | 2002-05-29 |
Family
ID=8236284
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98810846A Withdrawn EP0982089A1 (de) | 1998-08-27 | 1998-08-27 | Verfahren zur Prozessüberwachung beim Druckgiessen oder Thixoformen von Metallen |
| EP99944412A Expired - Lifetime EP1105237B1 (de) | 1998-08-27 | 1999-08-16 | Verfahren zur prozessüberwachung beim druckgiessen oder thixoformen von metallen |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98810846A Withdrawn EP0982089A1 (de) | 1998-08-27 | 1998-08-27 | Verfahren zur Prozessüberwachung beim Druckgiessen oder Thixoformen von Metallen |
Country Status (9)
| Country | Link |
|---|---|
| US (1) | US6557617B1 (de) |
| EP (2) | EP0982089A1 (de) |
| AT (1) | ATE218081T1 (de) |
| CA (1) | CA2341264A1 (de) |
| DE (1) | DE59901565D1 (de) |
| DK (1) | DK1105237T3 (de) |
| ES (1) | ES2176025T3 (de) |
| PT (1) | PT1105237E (de) |
| WO (1) | WO2000012246A1 (de) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US7886807B2 (en) * | 2007-06-15 | 2011-02-15 | Die Therm Engineering L.L.C. | Die casting control method |
| JP4889783B2 (ja) * | 2009-11-17 | 2012-03-07 | 日信工業株式会社 | 重力鋳造方法 |
| DE102010053125A1 (de) * | 2010-12-01 | 2012-06-06 | Volkswagen Ag | Verfahren zum Herstellen einer Serie von Gussbauteilen und Vorrichtung zum Herstellen eines Gussbauteils |
| DE102012220513B4 (de) | 2012-11-12 | 2023-02-16 | Bayerische Motoren Werke Aktiengesellschaft | Verfahren und Vorrichtung zur Herstellung eines Druckgussteils |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS57187154A (en) * | 1981-05-15 | 1982-11-17 | Toyota Motor Corp | Method and device for inspecting quality of product produced by die casting machine |
| US4493362A (en) * | 1982-05-27 | 1985-01-15 | Ex-Cell-O Corporation | Programmable adaptive control method and system for die-casting machine |
| ATE46843T1 (de) * | 1983-05-20 | 1989-10-15 | John Mickowski | Verfahren zum ueberwachen und steuern von periodisch arbeitenden form- und giessmaschinen und eine vorrichtung zur durchfuehrung dieses verfahrens. |
| US4976305A (en) * | 1987-12-01 | 1990-12-11 | Honda Giken Kogyo Kabushiki Kaisha | Method of and apparatus for controlling die temperature in low-pressure casting process |
| US5407000A (en) * | 1992-02-13 | 1995-04-18 | The Dow Chemical Company | Method and apparatus for handling molten metals |
| US5772933A (en) | 1994-10-12 | 1998-06-30 | Kotzab; Werner | Method for tempering an injection mold having at least one heated nozzle or hot runner |
| DE4444092C2 (de) * | 1994-10-12 | 1997-02-13 | Werner Kotzab | Verfahren und Anordnung zum Temperieren einer Spritzgießform mit wenigstens einer beheizten Düse oder einem Heißkanal |
| US5758707A (en) * | 1995-10-25 | 1998-06-02 | Buhler Ag | Method for heating metallic body to semisolid state |
| US6148899A (en) * | 1998-01-29 | 2000-11-21 | Metal Matrix Cast Composites, Inc. | Methods of high throughput pressure infiltration casting |
-
1998
- 1998-08-27 EP EP98810846A patent/EP0982089A1/de not_active Withdrawn
-
1999
- 1999-08-16 US US09/763,527 patent/US6557617B1/en not_active Expired - Fee Related
- 1999-08-16 DK DK99944412T patent/DK1105237T3/da active
- 1999-08-16 WO PCT/EP1999/006002 patent/WO2000012246A1/de not_active Ceased
- 1999-08-16 EP EP99944412A patent/EP1105237B1/de not_active Expired - Lifetime
- 1999-08-16 DE DE59901565T patent/DE59901565D1/de not_active Expired - Fee Related
- 1999-08-16 CA CA002341264A patent/CA2341264A1/en not_active Abandoned
- 1999-08-16 ES ES99944412T patent/ES2176025T3/es not_active Expired - Lifetime
- 1999-08-16 PT PT99944412T patent/PT1105237E/pt unknown
- 1999-08-16 AT AT99944412T patent/ATE218081T1/de not_active IP Right Cessation
Also Published As
| Publication number | Publication date |
|---|---|
| ES2176025T3 (es) | 2002-11-16 |
| WO2000012246A1 (de) | 2000-03-09 |
| EP1105237A1 (de) | 2001-06-13 |
| DE59901565D1 (de) | 2002-07-04 |
| CA2341264A1 (en) | 2000-03-09 |
| PT1105237E (pt) | 2002-09-30 |
| EP0982089A1 (de) | 2000-03-01 |
| ATE218081T1 (de) | 2002-06-15 |
| US6557617B1 (en) | 2003-05-06 |
| DK1105237T3 (da) | 2002-09-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69808295T2 (de) | Verfahren und vorrichtung zur oberflächentemperaturkontrolle eines blockes während des giessens und insbesondere während des angiessens | |
| DE69124657T2 (de) | Verfahren zur Beurteilung der Qualität von Druckgusstücken | |
| DE69308263T2 (de) | Schätzung der Metalltemperatur über die Abnutzung des Tauchrohres auf Grund des Eintauchens in Metallschmelze | |
| DE3887162T2 (de) | Giess- und eichsystem. | |
| EP1080809B1 (de) | Verfahren zur Regelung der Metalldosiermenge | |
| EP0982089A1 (de) | Verfahren zur Prozessüberwachung beim Druckgiessen oder Thixoformen von Metallen | |
| EP1072340B1 (de) | Verfahren zur Prozessüberwachung beim Druckgiessen oder Thixoformen von Metallen | |
| DE4103243A1 (de) | Verfahren zur steuerung des giessens einer fluessigkeit aus einem gefaess in einzelne gussformen sowie einrichtung zur durchfuehrung des verfahrens | |
| DE4208940C2 (de) | Verfahren und Vorrichtung zum Steuern des Haltedrucks beim Spritzgießen | |
| EP1070560A1 (de) | Verfahren zum Regeln der Kühlwasser-Durchflussgeschwindigkeit durch Kokillenbreitseiten | |
| EP0331612B1 (de) | Verfahren an einer Giessanlage zur Erzeugung von Strängen | |
| DE3424028C2 (de) | Verfahren zur Analyse der Zusammensetzung einer zweiphasigen Messingschmelze | |
| DE4203337A1 (de) | Verfahren zum Stranggießen von Metallen | |
| DE3009697C2 (de) | ||
| EP2460605B1 (de) | Verfahren zum Herstellen einer Serie von Gussbauteilen und Vorrichtung zum Herstellen eines Gussbauteils | |
| DE60212877T2 (de) | Vorrichtung zur herstellung von metallgussteilen | |
| CH646352A5 (en) | Apparatus for regulating the secondary cooling in a continuous-casting installation with batchwise smelt supply via a tundish | |
| DE69000282T2 (de) | Verfahren und vorrichtung zur herstellung von duennen metallprodukten mittels strangguss. | |
| EP1365873B1 (de) | Verfahren zum ermitteln von kenndaten eines oszillationssystems einer oszillierenden stranggiesskokille | |
| DE2821352A1 (de) | Verfahren und entsprechendes geraet fuer die voraussage metallographischer strukturen | |
| DE3706636C2 (de) | ||
| EP2266726A2 (de) | Verfahren zur Regelung der Flüssigkeitskühlung von Stranggießkokillen | |
| Venkatasamy | Analysis of in-cavity thermal and pressure characteristics in aluminum alloy die casting | |
| DE102019201249B4 (de) | Verfahren zur Einstellung einer Anfangsbedingung für Formungsprozessbedingungen | |
| DE102023106056A1 (de) | NIEDERDRUCKGIEßGEFÄß UND VERFAHREN ZUR STATUSBESTIMMUNG EINES NIEDERDRUCKGIEßGEFÄßES |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20010327 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: SI PAYMENT 20010327 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 20010731 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: ALCAN TECHNOLOGY & MANAGEMENT AG |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FI FR GB IE IT LI NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: SI PAYMENT 20010327 |
|
| REF | Corresponds to: |
Ref document number: 218081 Country of ref document: AT Date of ref document: 20020615 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 59901565 Country of ref document: DE Date of ref document: 20020704 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PT Payment date: 20020802 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20020820 Year of fee payment: 4 Ref country code: DK Payment date: 20020820 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20020826 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20020703 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20021009 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2176025 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20030303 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20030730 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20030806 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20030814 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030816 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030818 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20030818 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20030819 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20030820 Year of fee payment: 5 Ref country code: AT Payment date: 20030820 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20030828 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030901 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20030901 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040229 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MM4A Free format text: LAPSE DUE TO NON-PAYMENT OF FEES Effective date: 20040229 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040816 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040816 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040817 Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040831 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040831 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040831 |
|
| BERE | Be: lapsed |
Owner name: *ALCAN TECHNOLOGY & MANAGEMENT A.G. Effective date: 20040831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050301 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050301 |
|
| EUG | Se: european patent has lapsed | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20040816 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050429 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20050301 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050816 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20040817 |
|
| BERE | Be: lapsed |
Owner name: *ALCAN TECHNOLOGY & MANAGEMENT A.G. Effective date: 20040831 |