EP1036615A1 - Verfahren und Vorrichtung zum Aufschäumen eines metallischen Werkstoffes - Google Patents
Verfahren und Vorrichtung zum Aufschäumen eines metallischen Werkstoffes Download PDFInfo
- Publication number
- EP1036615A1 EP1036615A1 EP00105235A EP00105235A EP1036615A1 EP 1036615 A1 EP1036615 A1 EP 1036615A1 EP 00105235 A EP00105235 A EP 00105235A EP 00105235 A EP00105235 A EP 00105235A EP 1036615 A1 EP1036615 A1 EP 1036615A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- compact
- radiation
- protective layer
- wall
- room
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000034 method Methods 0.000 title claims abstract description 20
- 238000005187 foaming Methods 0.000 title claims abstract description 16
- 230000005855 radiation Effects 0.000 claims abstract description 31
- 239000011241 protective layer Substances 0.000 claims abstract description 25
- 239000010410 layer Substances 0.000 claims abstract description 24
- 239000011265 semifinished product Substances 0.000 claims abstract description 15
- 239000000843 powder Substances 0.000 claims abstract description 14
- 229910052751 metal Inorganic materials 0.000 claims abstract description 7
- 239000002184 metal Substances 0.000 claims abstract description 7
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N Silicium dioxide Chemical compound O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 claims description 22
- 239000000463 material Substances 0.000 claims description 22
- 229910018072 Al 2 O 3 Inorganic materials 0.000 claims description 11
- TWNQGVIAIRXVLR-UHFFFAOYSA-N oxo(oxoalumanyloxy)alumane Chemical compound O=[Al]O[Al]=O TWNQGVIAIRXVLR-UHFFFAOYSA-N 0.000 claims description 11
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 10
- 229910052782 aluminium Inorganic materials 0.000 claims description 8
- 239000006260 foam Substances 0.000 claims description 8
- 229910004298 SiO 2 Inorganic materials 0.000 claims description 6
- 238000006243 chemical reaction Methods 0.000 claims description 6
- XUIMIQQOPSSXEZ-UHFFFAOYSA-N Silicon Chemical compound [Si] XUIMIQQOPSSXEZ-UHFFFAOYSA-N 0.000 claims description 4
- 238000005566 electron beam evaporation Methods 0.000 claims description 4
- 238000007254 oxidation reaction Methods 0.000 claims description 4
- 230000008020 evaporation Effects 0.000 claims description 3
- 238000001704 evaporation Methods 0.000 claims description 3
- 238000007654 immersion Methods 0.000 claims description 3
- 238000005468 ion implantation Methods 0.000 claims description 3
- 238000001755 magnetron sputter deposition Methods 0.000 claims description 3
- 238000005240 physical vapour deposition Methods 0.000 claims description 3
- 229910052710 silicon Inorganic materials 0.000 claims description 3
- 239000010703 silicon Substances 0.000 claims description 3
- 238000005234 chemical deposition Methods 0.000 claims description 2
- 230000003647 oxidation Effects 0.000 claims description 2
- 239000012071 phase Substances 0.000 claims description 2
- 238000005289 physical deposition Methods 0.000 claims description 2
- 238000009832 plasma treatment Methods 0.000 claims description 2
- 239000012808 vapor phase Substances 0.000 claims description 2
- 239000003380 propellant Substances 0.000 claims 2
- 239000012778 molding material Substances 0.000 claims 1
- 238000007669 thermal treatment Methods 0.000 claims 1
- 239000004604 Blowing Agent Substances 0.000 abstract description 5
- 238000010438 heat treatment Methods 0.000 abstract description 4
- 239000008188 pellet Substances 0.000 description 7
- 239000002131 composite material Substances 0.000 description 6
- 239000007788 liquid Substances 0.000 description 5
- 238000012546 transfer Methods 0.000 description 4
- 239000000203 mixture Substances 0.000 description 3
- 239000011148 porous material Substances 0.000 description 3
- 230000005540 biological transmission Effects 0.000 description 2
- 238000000576 coating method Methods 0.000 description 2
- 239000011521 glass Substances 0.000 description 2
- 230000008018 melting Effects 0.000 description 2
- 238000002844 melting Methods 0.000 description 2
- 238000013021 overheating Methods 0.000 description 2
- 238000005096 rolling process Methods 0.000 description 2
- 230000003595 spectral effect Effects 0.000 description 2
- 230000000007 visual effect Effects 0.000 description 2
- 230000001464 adherent effect Effects 0.000 description 1
- 239000002318 adhesion promoter Substances 0.000 description 1
- 230000002411 adverse Effects 0.000 description 1
- AZDRQVAHHNSJOQ-UHFFFAOYSA-N alumane Chemical group [AlH3] AZDRQVAHHNSJOQ-UHFFFAOYSA-N 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000000919 ceramic Substances 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 238000007796 conventional method Methods 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 230000008878 coupling Effects 0.000 description 1
- 238000010168 coupling process Methods 0.000 description 1
- 238000005859 coupling reaction Methods 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
- 230000007774 longterm Effects 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 239000007769 metal material Substances 0.000 description 1
- 239000010453 quartz Substances 0.000 description 1
- 239000011863 silicon-based powder Substances 0.000 description 1
- 239000011343 solid material Substances 0.000 description 1
- -1 titanium hydride Chemical compound 0.000 description 1
- 229910000048 titanium hydride Inorganic materials 0.000 description 1
- 239000012780 transparent material Substances 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/10—Sintering only
- B22F3/105—Sintering only by using electric current other than for infrared radiant energy, laser radiation or plasma ; by ultrasonic bonding
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/10—Sintering only
- B22F3/11—Making porous workpieces or articles
- B22F3/1121—Making porous workpieces or articles by using decomposable, meltable or sublimatable fillers
- B22F3/1125—Making porous workpieces or articles by using decomposable, meltable or sublimatable fillers involving a foaming process
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F27—FURNACES; KILNS; OVENS; RETORTS
- F27B—FURNACES, KILNS, OVENS OR RETORTS IN GENERAL; OPEN SINTERING OR LIKE APPARATUS
- F27B17/00—Furnaces of a kind not covered by any of groups F27B1/00 - F27B15/00
- F27B17/0016—Chamber type furnaces
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2998/00—Supplementary information concerning processes or compositions relating to powder metallurgy
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F27—FURNACES; KILNS; OVENS; RETORTS
- F27D—DETAILS OR ACCESSORIES OF FURNACES, KILNS, OVENS OR RETORTS, IN SO FAR AS THEY ARE OF KINDS OCCURRING IN MORE THAN ONE KIND OF FURNACE
- F27D99/00—Subject matter not provided for in other groups of this subclass
- F27D99/0001—Heating elements or systems
- F27D99/0006—Electric heating elements or system
- F27D2099/0028—Microwave heating
Definitions
- the invention relates to a method for foaming at least one a metal powder and at least one gas-releasing blowing agent powder Semi-finished product, which is optionally connected to at least one cover layer, the semi-finished product is introduced into a room and heated to foam it becomes.
- the invention further relates to a device for foaming a from at least one metal powder and at least one gas-releasing blowing agent powder existing semi-finished product, which may be provided with a top layer, comprising a space which receives the compact and is delimited by a wall, and a heat source for thermal foaming of the compact Treatment of the compact in the room.
- DE 44 26 627 C2 describes a method and a device for producing metallic composite materials made of one or more outer layers made of solid Material and known from a core located between them, by compression a mixture of at least one metal powder and at least one gas-releasing blowing agent powder is formed. A composite thus formed is then placed in a chamber furnace at a temperature of 850 ° C. At this temperature The compact foams to the required extent without the cover layers melt.
- the heating is therefore carried out by heat transfer such that initially over the furnace indirectly transfers the heat to the compact via a foam tool becomes.
- Such a process is energetically unfavorable and often leads to overheating of the foam so that the composite materials produced are not the required ones Exhibit goodness.
- the present invention is based on the problem, a method and a Arrangement of the type mentioned in such a way that with high efficiency and energetically favorable compacts can be foamed, the additional Possibility should be given to different areas of the compact differently to warm up or, if necessary, observe the foaming in order to intervene in a targeted manner to be able to.
- the problem is essentially solved in that the semi-finished product is foamed by radiation energy injected into the room from the outside.
- the semi-finished product is foamed by radiation energy injected into the room from the outside.
- Radiating from the known prior art there is no heat transfer from the room that receives the pellet itself, but from outside into the room coupled energy. This is particularly radiation energy in the middle or far infrared range. Radiation in the microwave range also comes in Question.
- the pellet is heated in a room by one for the one to be coupled Radiation transparent or semi-transparent or translucent wall is limited, the room side with a foamable pellet and the optionally present top layer chemically inert to the coupled radiant energy permeable or substantially permeable Protective layer is provided.
- the wall of the room that receives the compact the protective layer is applied comes in particular quartz glass material or containing such in question.
- Al 2 O 3 and / or Si 3 N 4 and / or BN and / or SiO 2 / Al 2 O 3 and / or mixtures thereof can be used as the protective layer.
- the protective layer can be applied to the inner surfaces of the wall, possibly via an adhesion promoter layer, by means of PVD processes. Electron beam evaporation, magnetron sputtering, cathodic arc evaporation or plasma immersion ion implantation are particularly suitable.
- the protective layer such as aluminum oxide layer is coupled to the wall such as the quartz glass component via at least one graded intermediate layer, in particular made of silicon and aluminum oxide, in particular the protective layer such as aluminum oxide layer by physical deposition from the vapor phase and / or by chemical deposition from the gas phase is deposited and preferably the aluminum oxide is formed by post-oxidation of an aluminum layer by means of plasma treatment and / or thermal oxidation or reaction with SiO 2 .
- a device of the type mentioned is characterized in that the wall from radiation energy of the energy source that can be coupled into the room or is at least translucent and inside the room with one opposite foamable material chemically inert and against radiation energy transparent or translucent protective layer is covered.
- the wall itself built especially on quartz glass. So the wall can be made up of individual Glass blocks exist, whereby a modular structure of the room is possible, so that its inner geometry easily matches the final geometry of the foam to be foamed Body is customizable.
- the thickness D of the wall itself should be in the range between 5 and 25 mm, in particular be about 15 mm.
- the heat source itself is preferably an IR radiator, the Radiation energy can be coupled in such a way that it is in the body to be foamed Can form heat sinks. This enables a specific foaming geometry and targeted density gradients can be achieved.
- the protective layer which, as mentioned, can be an Al 2 O 3 or Si 3 N 4 or BN material or contain it, it should be noted that its thickness is in the range between 20 nm and 2 ⁇ m.
- the teachings of the invention are radiant heat with a structurally simple structure can be coupled into the pellet or body to be foamed, whereby compared to conventional methods, in which heat transfer by means of there is considerable energy savings from the heat given off by the furnace walls and in particular results in a time saving of up to 50%. Overheating the foam is excluded. There is also no post-heating, which means the cycle times of foaming would otherwise be adversely affected.
- the radiation energy that can be coupled in also has the advantage that areas heat can be applied to the semi-finished product to be foamed, so that, as mentioned, a desired geometry formation is already achieved by foaming can be done.
- quartz glass material By using quartz glass material to form the walls that the surrounding the foam to be foamed, mechanically stressable long-term stable Materials used that are inexpensive to manufacture and use can.
- the quartz glass ensures that heat radiation, especially in the Infrared range up to 2 ⁇ m and in the range between 3 and 3.5 ⁇ m with a transmission coefficient can be coupled in between 0.8 and 0.9.
- the Use of quartz glass the possibility of visual observation when foaming, so that a controlling intervention when foaming is possible.
- the wall can preferably consist of quartz glass components. Is quartz glass because of its high melting point and high transparency in the infrared and Visible spectral range for coupling heat radiation into hot, liquid and gaseous media and suitable for observing the processes themselves. On contact however, reactions occur with chemically aggressive media such as liquid aluminum on, the quartz glass parts or components made from them within a short time to destroy.
- the transparent glass block faces the material Side is chemically passivated and provided with a protective layer made of aluminum oxide. It can have a thickness between 20 nm and 2 ⁇ m.
- the aluminum oxide layer from a graded intermediate layer Silicon and / or aluminum oxide is coupled to the base material.
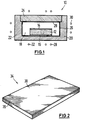
- a device 10 is shown in which a semifinished product 12, the opposite Sides are provided with metal cover layers 14, 16, to be foamed to form a metallic composite material of low weight, but to produce high strength.
- Corresponding composite materials form powerful ones Lightweight structures that e.g. B. used in traffic engineering. Such composites are characterized by low density and relatively high Stiffness.
- the semi-finished product 12 can be made from a mixture of aluminum powder and z. B. 12% by weight Silicon powder and 0.8% by weight titanium hydride powder as gas-releasing Blowing agent powder be composed, which then mixes pre-compacted into an ingot become. This can be open or closed pore. Then there is the pellet 12 have been covered with the cover layers 14, 16 by rolling. If the pellet 12 was open-pore, this process step becomes a necessary closed-pore achieved. The temperature during rolling itself is approximately 400 ° C.
- the sandwich body thus formed is then introduced into a space 18, which is from a wall 20 is limited, which consists of quartz glass material.
- a space which is from a wall 20 is limited, which consists of quartz glass material.
- the space is made up of a pot-shaped lower part 22 and a closing part Cover part 24 formed.
- a Protective layer 26, 28 provided, the radiation to be coupled into the room 18 is permeable.
- the thickness of the wall 20 itself is also chosen such that this is transparent or translucent to a coupling-in radiation.
- the receptacle is surrounded on the circumference by infrared radiators, which are provided with the reference numerals 30, 32 by way of example.
- the protective layer 26 is preferably one made of Al 2 O 3 , Si 3 N 4 , BN or SiO 2 / Al 2 O 3 or containing these materials.
- the protective layer is chemically inert to the aggressive material of the compact, in particular when aluminum powder is used, so that the quartz material that is otherwise attackable by aluminum is protected.
- the thickness of the protective layer 26, 28 is selected such that it is also transparent or translucent to radiation to be coupled in. Radiation can thus be coupled into the space 18 from the outside to the required extent in order to heat the compact 12 to a temperature which enables foaming.
- the infrared radiators 30, 32 can be arranged around the space 18 in such a way that heat sinks can form in the pellet 12, as a result of which specific geometry and / or density gradients can be achieved when foaming.
- the space 18 can furthermore have an internal geometry, that of the final geometry of the workpiece to be foamed.
- a simple geometry adjustment to enable, the walls 20 can be modular, so that change is possible with simple measures.
- the protective layers 26, 28 are preferably made by PVD methods, in particular by electron beam evaporation, magnetron sputtering, arc evaporation or Plasma immersion ion implantation applied.
- the protective layer 26, 28 adequately protects the quartz glass material, its should Thickness between 5 and 25 nm, in particular in the range of 10 nm.
- the wall itself has a thickness D of 15 mm.
- Light in the middle infrared range is preferably emitted by the emitters 30, 32. Regardless, however, the wavelength should be based on the material of the wall and the Protective layer must be coordinated to ensure a high degree of transmission.
- a z. B. shown for a mold arrangement bottom plate 34 made of quartz glass, the z. B. Dimension of 180x80x5 mm 3 .
- the plate 34 has an approximately 1 ⁇ m thick and adherent layer 38 made of Al 2 O 3 on its inner surface 36 of the mold. Electron beam evaporation from an Al 2 O 3 melt can be used as the coating process. The coating takes place at a residual gas pressure of approximately 1 x 10 -4 mbar.
- the corresponding plate 34 can be provided with the layer 38 in a mold, not shown be used facing the interior. Both when pouring liquid aluminum as well as when melting an aluminum sheet using infrared radiation is coupled through the transparent plate 36, a reaction with the Quartz glass plate 34 liquid aluminum can not be found. After cooling could freeze a solidified aluminum part from the coated quartz glass plate 34 can be removed.
- the mold itself can be arranged in a carrier receptacle for transport to a heat source such as infrared radiators or away from them.
- a heat source such as infrared radiators or away from them.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- General Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Surface Treatment Of Glass (AREA)
- Laminated Bodies (AREA)
- Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
- Manufacture Of Porous Articles, And Recovery And Treatment Of Waste Products (AREA)
Abstract
Description
- Fig. 1
- eine Vorrichtung zum Herstellen eines aufschäumbaren metallischen Werkstoffes und
- Fig. 2
- eine beschichtete Quarzglasplatte.
Claims (13)
- Verfahren zum Aufschäumen eines aus zumindest einem Metallpulver und zumindest einem gasabspaltenden Treibmittelpulver bestehenden Halbzeugs, das gegebenenfalls mit zumindest einer Deckschicht verbunden wird, wobei das Halbzeug in einem Raum eingebracht und zu dessen Aufschäumen erwärmt wird,
dadurch gekennzeichnet,
dass das Halbzeug durch von außen in den Raum eingekoppelte Strahlungsenergie aufgeschäumt wird. - Verfahren nach Anspruch 1,
dadurch gekennzeichnet,
dass der Pressling in einem Raum erwärmt wird, der von einer transparenten, semitransparenten bzw. translucenten Wandung begrenzt ist, die zumindest rauminnenseitig mit einer gegenüber dem aufschäumbaren Pressling und der gegebenenfalls vorhandenen Deckschicht chemisch inerten, gegenüber der angekoppelten Strahlungsenergie durchlässigen oder im Wesentlichen durchlässigen Schutzschicht versehen wird. - Verfahren nach zumindest Anspruch 1 oder 2,
dadurch gekennzeichnet,
dass der Pressling mit einer Strahlung einer Wellenlänge λ mit 700 nm < λ < 4 µm, insbesondere mit 3,0 < λ < 3,5 µm, oder mit einer Strahlung im mittleren Infrarot oder mit einer Strahlung, die im fernen Infrarot liegt, oder mit einer Strahlung im Mikrowellenbereich erwärmt wird. - Verfahren nach zumindest einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass als Wandung des den Pressling aufnehmenden Raums in Bezug auf die einzukoppelnde Strahlung transparentes bzw. semitransparentes Formmaterial wie Quarzglasmaterial oder solches enthaltendes verwendet wird. - Verfahren nach zumindest einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass als Schutzschicht Al2O3 und/oder Si3N4 und/oder Al2O3/SiO2 und/oder BN oder diese enthaltendes Material verwendet wird, wobei vorzugsweise die Schutzschicht mit einer Dicke d mit 8 nm ≤ d ≤ 2 µm, insbesondere d in etwa 20 um bis 500 nm versehen wird. - Verfahren nach zumindest einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass die Schutzschicht durch PVD-Verfahren, durch Elektronenstrahlverdampfung, Magnetron-Sputtern, Lichtbogenverdampfung oder Plasmaimmersions-Ionenimplantation aufgebracht wird. - Verfahren nach zumindest einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass die Strahlungsenergie derart angekoppelt wird, dass sich im Pressling Wärmesenken bilden. - Verfahren nach zumindest einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass die Schutzschicht wie Aluminiumoxidschicht (38) über zumindest eine gradierte Zwischenschicht insbesondere aus Silicium- und Aluminiumoxid an die Wandung wie das Quarzglasbauteil (34) angekoppelt wird, dass insbesondere die Schutzschicht wie Aluminiumoxidschicht durch physikalische Abscheidung aus der Dampfphase und/oder durch chemische Abscheidung aus der Gasphase abgeschieden wird und dass vorzugsweise das Aluminiumoxid durch Nachoxidation einer Aluminiumschicht mittels Plasmabehandlung und/oder thermische Oxidation bzw. Reaktion mit SiO2 ausgebildet wird. - Vorrichtung zum Aufschäumen eines aus zumindest einem Metallpulver und zumindest einem gasabspaltenden Treibmittelpulver bestehenden Halbzeugs (12), das gegebenenfalls mit zumindest einer Deckschicht (14, 16) verbunden ist, umfassend einen den Pressling aufnehmenden von einer Wandung (20) begrenzten Raum (18) sowie eine Wärmequelle zum Aufschäumen des Presslings durch thermische Behandlung des Presslings in dem Raum,
dadurch gekennzeichnet,
dass die Wandung (20, 22, 24) gegenüber in dem Raum (18) einkoppelbarer Strahlungsenergie der Energiequelle (30, 32) transparent oder zumindest translucent ist und zumindest rauminnenseitig mit einer gegenüber dem aufschäumbaren Material chemisch inerten und gegenüber der Strahlungsenergie transparenten oder translucenten Schutzschicht (26, 28) abgedeckt ist. - Vorrichtung nach Anspruch 9,
dadurch gekennzeichnet,
dass die Wandung (20, 22, 24) auf Quarzglasbasis, insbesondere in Form von Quarzglasbausteinen aufgebaut ist, wobei die Wandung (20, 22, 24) gegebenenfalls modular aufgebaut ist, und dass die Wandung vorzugsweise eine Dicke D mit 5 mm ≤ D ≤ 25 mm, insbesondere mit D in etwa 15 mm aufweist. - Vorrichtung nach zumindest einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass die Schutzschicht (26, 28) aus Al2O3 und/oder SiO2/Al2O3 und/oder Si3N4 und/oder BN besteht oder dieses enthält und vorzugsweise eine Dicke d mit 20 nm ≤ d ≤ 2 µm aufweist. - Vorrichtung nach zumindest einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass die Wärmequelle (30, 32) insbesondere zumindest ein IR-Strahler ist und dass vorzugsweise die Wärmequelle derart außerhalb des Raumes (18) angeordnet ist, dass in dem Pressling (12) Wärmesenken ausbildbar sind. - Vorrichtung nach zumindest einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass der Pressling in einer von den Wandungen (20, 22, 24) gebildeten Kokille anordbar ist, die in einer Trägeraufnahme angeordnet ist.
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19911228 | 1999-03-13 | ||
| DE19911228 | 1999-03-13 | ||
| DE19954755 | 1999-11-15 | ||
| DE1999154755 DE19954755A1 (de) | 1999-11-15 | 1999-11-15 | Verfahren und Vorrichtung zum Aufschäumen eines metallischen Werkstoffes |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1036615A1 true EP1036615A1 (de) | 2000-09-20 |
| EP1036615B1 EP1036615B1 (de) | 2005-05-25 |
Family
ID=26052347
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP00105235A Expired - Lifetime EP1036615B1 (de) | 1999-03-13 | 2000-03-13 | Verfahren zum Aufschäumen eines metallischen Werkstoffes |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP1036615B1 (de) |
| AT (1) | ATE296179T1 (de) |
| DE (1) | DE50010372D1 (de) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3165307A1 (de) * | 2015-11-03 | 2017-05-10 | Havel metal foam GmbH | Verfahren und vorrichtung zur herstellung von metallschaumverbundkörpern und metallschaumverbundkörper |
| EP3653740A4 (de) * | 2017-07-14 | 2020-12-30 | Japan Science and Technology Agency | Verfahren zur herstellung von metallschaum und vorrichtung zur herstellung von metallschaum |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5699683A (en) * | 1980-01-14 | 1981-08-11 | Maruzen Kk | Method of forming braille or the like |
| DE4413423A1 (de) * | 1994-04-18 | 1995-10-19 | Paar Anton Kg | Vorrichtung zum Aufschluß von Substanzen |
| EP0726127A1 (de) * | 1995-02-02 | 1996-08-14 | Hüls Aktiengesellschaft | Formen zur Herstellung von geformten Artikeln aus Latexschaum mittels Mikrowellenenergie |
| DE19734394A1 (de) * | 1996-08-13 | 1998-02-26 | Friedrich Wilhelm Bessel Inst | Vorrichtung und Verfahren zur Herstellung von Metallschaum |
| AT406558B (de) * | 1998-05-27 | 2000-06-26 | Illichmann Gmbh Leichtmetallgu | Verfahren und vorrichtung zum herstellen von metallschaumteilen |
-
2000
- 2000-03-13 DE DE50010372T patent/DE50010372D1/de not_active Expired - Fee Related
- 2000-03-13 AT AT00105235T patent/ATE296179T1/de not_active IP Right Cessation
- 2000-03-13 EP EP00105235A patent/EP1036615B1/de not_active Expired - Lifetime
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5699683A (en) * | 1980-01-14 | 1981-08-11 | Maruzen Kk | Method of forming braille or the like |
| DE4413423A1 (de) * | 1994-04-18 | 1995-10-19 | Paar Anton Kg | Vorrichtung zum Aufschluß von Substanzen |
| EP0726127A1 (de) * | 1995-02-02 | 1996-08-14 | Hüls Aktiengesellschaft | Formen zur Herstellung von geformten Artikeln aus Latexschaum mittels Mikrowellenenergie |
| DE19734394A1 (de) * | 1996-08-13 | 1998-02-26 | Friedrich Wilhelm Bessel Inst | Vorrichtung und Verfahren zur Herstellung von Metallschaum |
| AT406558B (de) * | 1998-05-27 | 2000-06-26 | Illichmann Gmbh Leichtmetallgu | Verfahren und vorrichtung zum herstellen von metallschaumteilen |
Non-Patent Citations (2)
| Title |
|---|
| DATABASE WPI Section Ch Week 200010, Derwent World Patents Index; Class M13, AN 2000-106574, XP002141265 * |
| PATENT ABSTRACTS OF JAPAN vol. 005, no. 174 (M - 096) 10 November 1981 (1981-11-10) * |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3165307A1 (de) * | 2015-11-03 | 2017-05-10 | Havel metal foam GmbH | Verfahren und vorrichtung zur herstellung von metallschaumverbundkörpern und metallschaumverbundkörper |
| EP3653740A4 (de) * | 2017-07-14 | 2020-12-30 | Japan Science and Technology Agency | Verfahren zur herstellung von metallschaum und vorrichtung zur herstellung von metallschaum |
| US11623274B2 (en) | 2017-07-14 | 2023-04-11 | Japan Science And Technology Agency | Metal foam production method and metal foam production apparatus |
Also Published As
| Publication number | Publication date |
|---|---|
| DE50010372D1 (de) | 2005-06-30 |
| EP1036615B1 (de) | 2005-05-25 |
| ATE296179T1 (de) | 2005-06-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0887438B1 (de) | Verfahren zur Oberflächenvergütung innerer Oberflächen von Hohlkörpern und Vorrichtung zur Durchführung des Verfahrens | |
| DE4408250C2 (de) | Oberflächenschichtsystem für Substrate | |
| DE69613822T3 (de) | Verfahren zur vakuumaufkohlung, verwendung einer vorrichtung zur vakuumaufkohlung und aufgekohlte stahlerzeugnisse | |
| EP0118702B1 (de) | Verfahren zur Herstellung eines Gegenstandes aus pulverförmigem Material durch isostatisches Pressen | |
| EP2475797B1 (de) | Verfahren und vorrichtung zum härten von werkstücken | |
| WO1998050599A2 (de) | Quarzglas-bauteil für ein reaktorgehäuse sowie herstellungsverfahren und anwendung dafür | |
| EP2212446A1 (de) | Oxidverbindungen als beschichtungszusammensetzung | |
| EP1829843B1 (de) | Vorrichtung zum behandeln von werkstücken aus porösem kohlenstoff-material | |
| EP0911426A1 (de) | Herstellung von Formteilen | |
| EP1608476B1 (de) | Verfahren und vorrichtung zur herstellung von massgenauem schaum | |
| DE102007049930A1 (de) | Oberflächenmodifizierte Strukturen | |
| EP2437020B1 (de) | Mikrowellenofen | |
| DE60021302T2 (de) | Verfahren und Vorrichtung zur Behandlung eines Werkstoffes mit elektromagnetischer Strahlung in einer kontrollierten Atmosphäre | |
| EP1036615B1 (de) | Verfahren zum Aufschäumen eines metallischen Werkstoffes | |
| DE10041582B4 (de) | Quarzglastiegel sowie Verfahren zur Herstellung desselben | |
| EP3411516B1 (de) | Tiegel | |
| DE3401700C1 (de) | Verfahren zur Herstellung von Pulvern unter Weltraumbedingungen | |
| DE19954755A1 (de) | Verfahren und Vorrichtung zum Aufschäumen eines metallischen Werkstoffes | |
| DE19928997C2 (de) | Verfahren und Vorrichtung zum Schäumen von Metallen | |
| DE102004002303B4 (de) | Verfahren zur Herstellung eines beschichteten Kohlenstoff/Kohlenstoff-Verbundwerkstoffes und danach hergestellter beschichteter Kohlenstoff/Kohlenstoff-Verbundwerkstoff | |
| DE4432730A1 (de) | Verfahren zur Herstellung einer metallischen Struktur | |
| DE4413423A1 (de) | Vorrichtung zum Aufschluß von Substanzen | |
| DE69404669T2 (de) | Verfahren zur verdichtung einer porösen struktur mit bornitrid | |
| EP4232213B1 (de) | Verwendung einer plasmapolymeren schicht als trennschicht im nicht-eisen-metallguss | |
| EP1133579B1 (de) | Verfahren zur herstellung einer schutzschicht auf einem martensitischen stahl und verwendung des mit der schutzschicht versehenen stahls |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20000927 |
|
| AKX | Designation fees paid |
Free format text: AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| 17Q | First examination report despatched |
Effective date: 20030422 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RTI1 | Title (correction) |
Free format text: PROCESS FOR FOAMING METALLIC ARTICLES |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SCHUNK SINTERMETALL GMBH |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRE;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED.SCRIBED TIME-LIMIT Effective date: 20050525 Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050525 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050525 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050525 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050525 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50010372 Country of ref document: DE Date of ref document: 20050630 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050825 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050825 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050825 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050905 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051027 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20050525 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20060329 Year of fee payment: 7 Ref country code: DE Payment date: 20060329 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060331 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060331 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060331 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060331 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060331 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20060228 |
|
| EN | Fr: translation not filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070313 |
|
| BERE | Be: lapsed |
Owner name: SCHUNK SINTERMETALL G.M.B.H. Effective date: 20060331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20071002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050525 Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050525 |