EP1008667B1 - Verfahren zur Herstellung feuerresistenter Stahlbleche - Google Patents
Verfahren zur Herstellung feuerresistenter Stahlbleche Download PDFInfo
- Publication number
- EP1008667B1 EP1008667B1 EP99123536A EP99123536A EP1008667B1 EP 1008667 B1 EP1008667 B1 EP 1008667B1 EP 99123536 A EP99123536 A EP 99123536A EP 99123536 A EP99123536 A EP 99123536A EP 1008667 B1 EP1008667 B1 EP 1008667B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- yield strength
- temperature
- strip
- sheets
- steel
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/26—Ferrous alloys, e.g. steel alloys containing chromium with niobium or tantalum
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/26—Methods of annealing
- C21D1/28—Normalising
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0221—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the working steps
- C21D8/0226—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/24—Ferrous alloys, e.g. steel alloys containing chromium with vanadium
Definitions
- the invention relates to a method for producing fire-resistant steel sheets with a yield strength Re> 235 N / mm 2 and a yield strength ratio Re / Rm (yield strength R e; tensile strength R m ) between 0.4 and 0.65, in particular between 0.4 and 0.6, for use in steel construction.
- Fire resistant steels must have high heat resistance have, so in steel construction a reduction of expensive Fire protection measures is made possible. At the same time a fire resistant steel to achieve a good one Deformation behavior a very low yield ratio Show Re / Rm. This increases the security of the Construction against mechanical failure Burden.
- the steels to be created according to the invention also have the construction steel for steel structures requirements regarding To meet toughness and processing behavior and increased resistance to atmospheric corrosion To have (weather resistance).
- the critical temperature is reached when the at this temperature measured yield point below 2/3 of the yield point measured at room temperature has sunk.
- Conventional structural steels have about 350 ° C their critical temperature. Because of the need expensive fire protection measures for conventional structural steels Having to undertake to a considerable extent is one Inexpensive construction work is not guaranteed and a optimal use of space is often difficult.
- the object of the present invention is now based on an inexpensive method of manufacture to propose steels with which fire protection measures by a critical over the state of the art Temperature can be further reduced and the improved ductility due to a low yield ratio have from 0.4 to 0.65. hereby is supposed to be an inexpensive and modern building design high security against mechanical and thermal Construction failure enabled and in parallel increased resistance to atmospheric corrosion be created.
- the C content in a range of 0.01 to 0.12% and the Mn content in a range from 0.20 to 1.00% be limited.
- This steel becomes slabs in free-standing or continuous casting or shed thin slabs.
- the slabs are made with a Starting temperature in the range from 1000 to 1350 ° C Hot rolled strips. In the case of slab production these are at the hot rolling start temperature heated. On the other hand, if thin slabs are poured, these can be removed from the pouring heat after cooling to the Hot rolling start temperature immediately afterwards the casting process can be further processed by Strips are rolled out.
- the hot rolling final temperature is above 850 ° C, preferred however not higher than 900 ° C.
- the hot rolled strips with thicknesses up to max. 15 mm cool down after the outlet the hot rolling season only in air at a temperature in the range of 720 to 780 ° C coiled, which is particularly good in practice Set results.
- According to an embodiment of the Invention can limit the reel temperature at 760 ° C. After the reel are removed from the tapes Plate removed.
- the sheets thus produced are advantageously in the Temperature range from 880 to 950 ° C, preferably at 920 ° C, normalized for a maximum of 30 minutes.
- the sheets can then also in the temperature range of 400 ° C. tempered up to 700 ° C.
- the inventive method is in the Sheet steel creates a multi-phase structure that predominantly made of ferrite with embedded bainitic / martensitic islands and above also has finely divided carbide deposits. On this structure is based on the high heat resistance and that low yield ratio as a prerequisite for good ductility of the sheets.
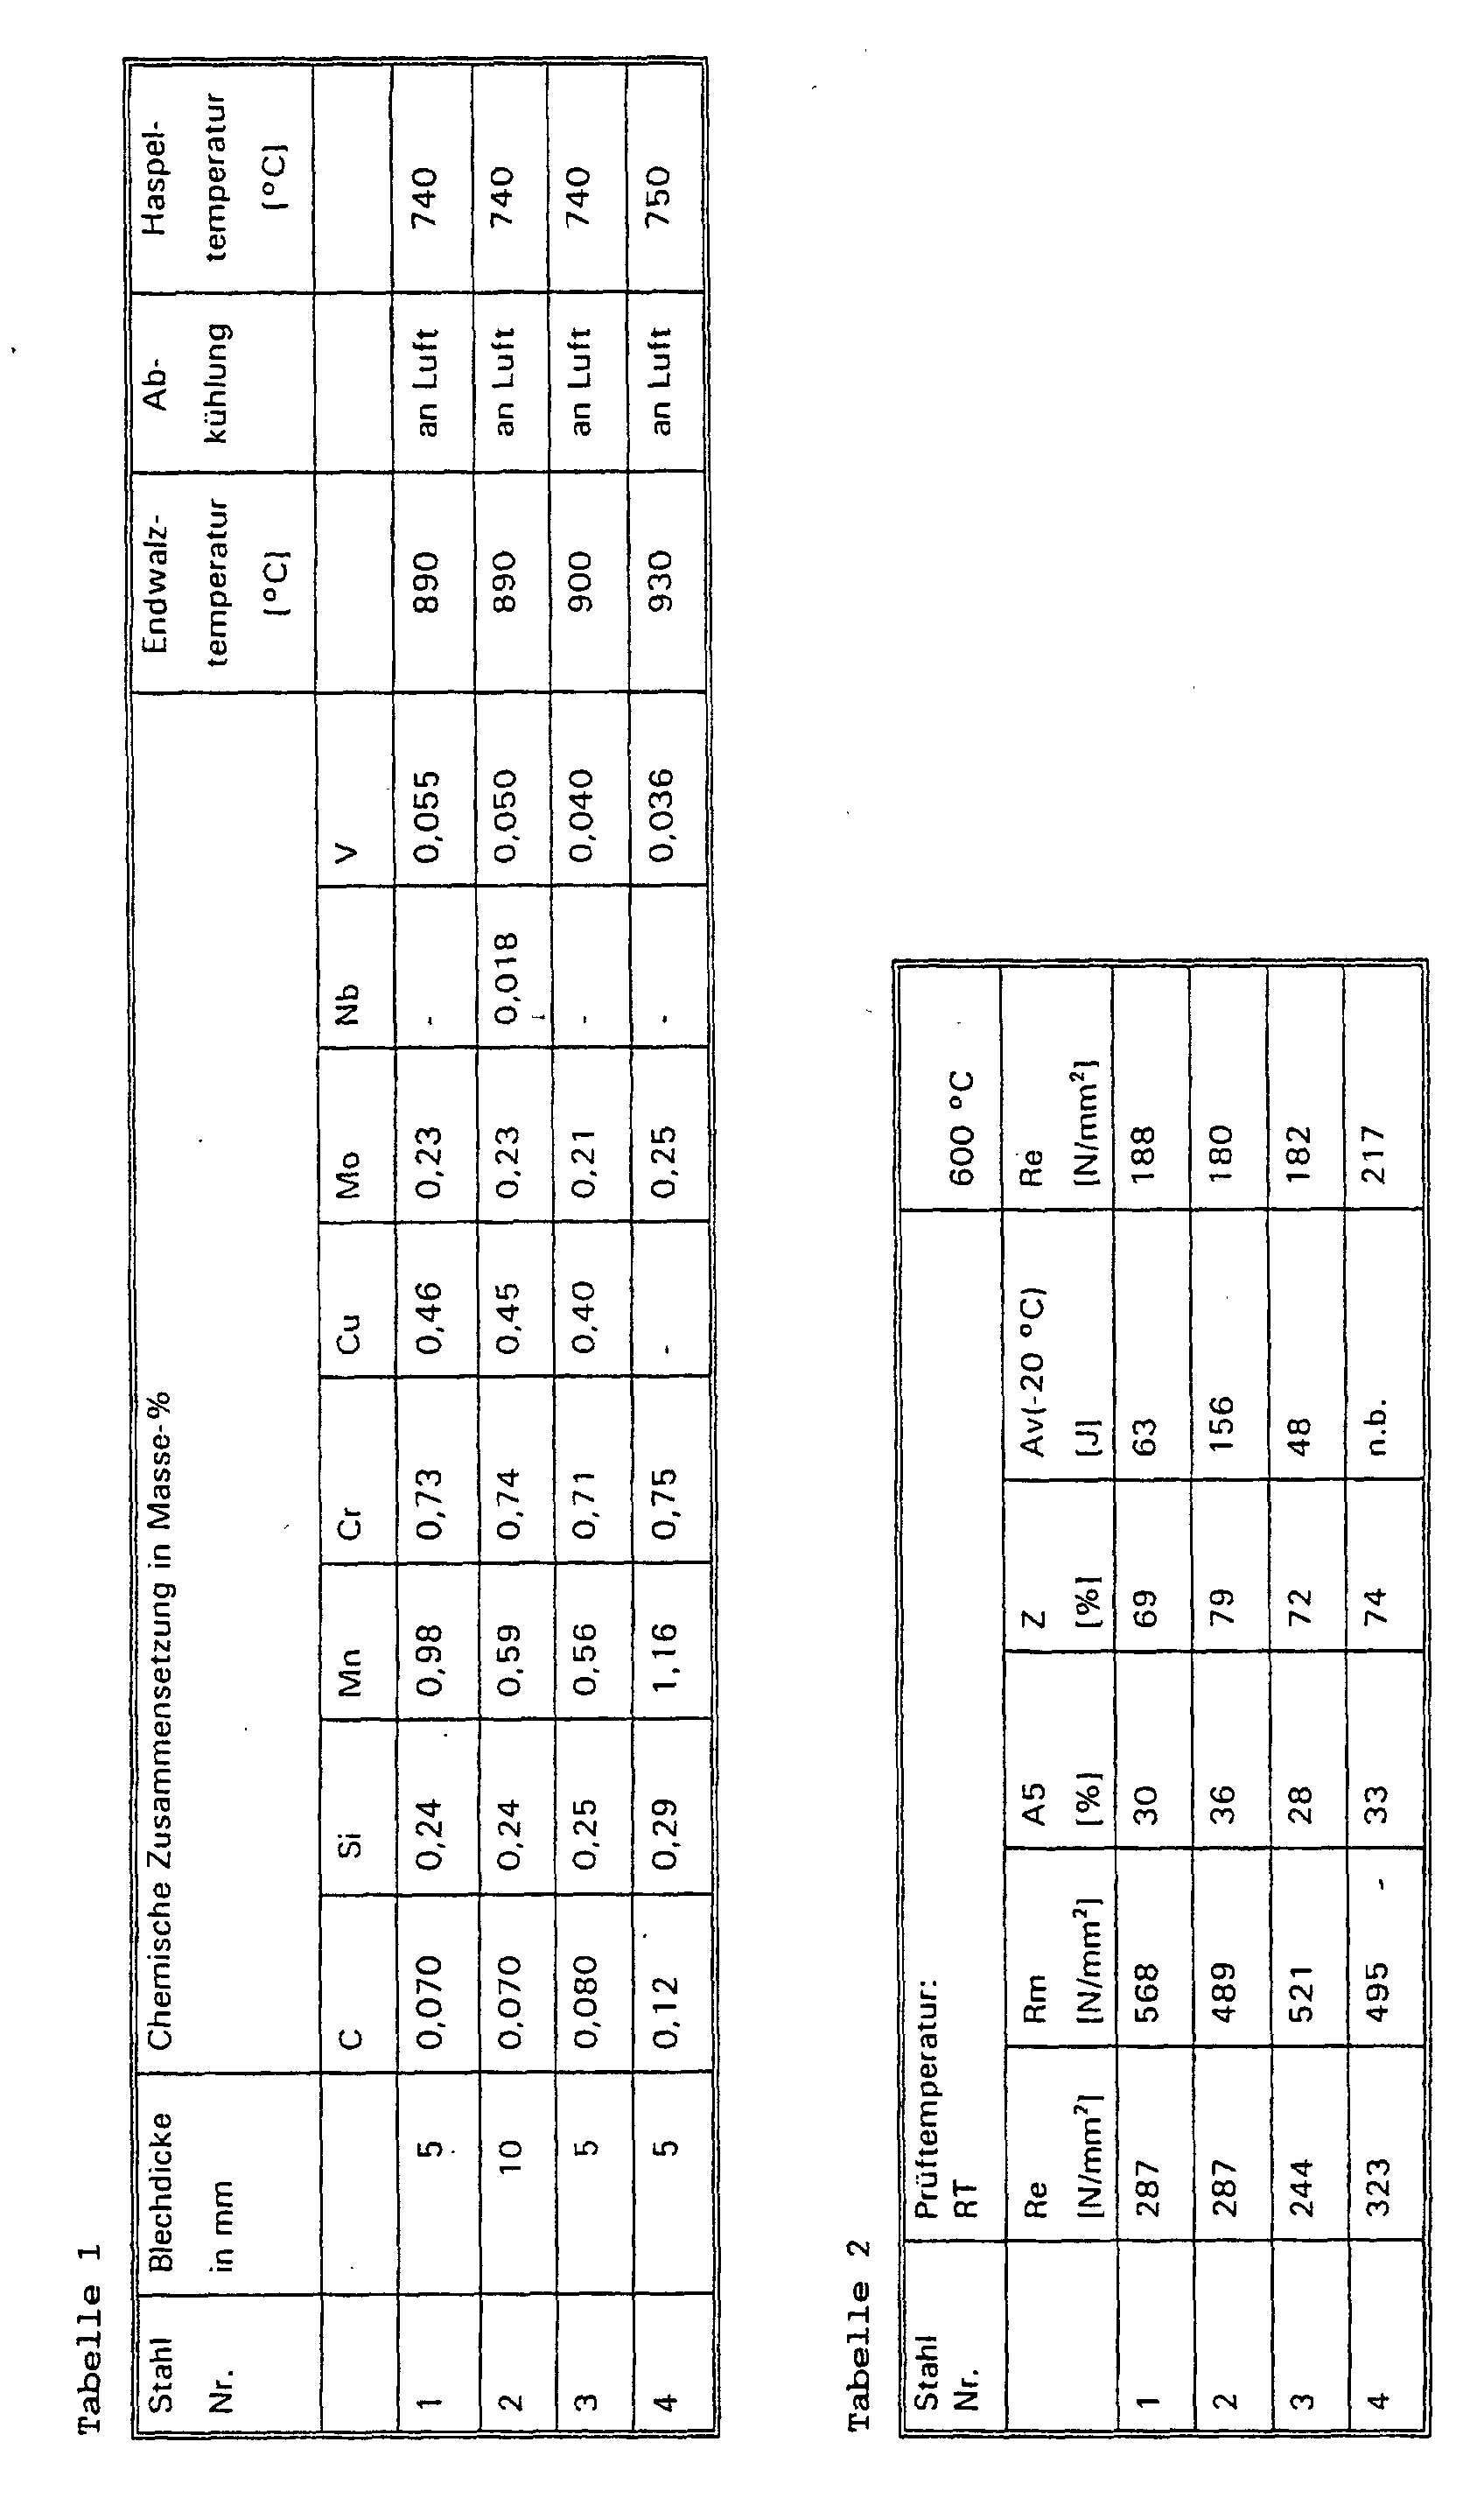
- Table 1 lists the chemical compositions of fire-resistant nickel-free steels 1 - 4 in the form of 5 and 10 mm thick sheet metal as well as the final rolling and coiling temperatures observed during the processing of the steels.
- the steels were cast into slabs, which were then heated to 1200 ° C and hot rolled into strip, the in Table 1 given respective final rolling temperatures have been achieved. Starting from the respective The final rolling temperature was the respective strip in air the respective reel temperature given in Table 1 cooled. Then sheets were removed from the strips with a normal annealing at 920 ° C have been subjected to a holding time of less than 30 minutes.
- Table 2 contains the mechanical properties measured on samples of the sheets from the fire-resistant nickel-free steels 1 - 4 of the composition according to Table 1. Characteristic is in particular the significantly higher heat resistance, which is characterized here by the yield strength Re at 600 ° C, which is between 180 and 217 N / mm 2 . This corresponds to a yield point reduction compared to room temperature of more than 3/5. This can raise the critical temperature to over 600 ° C and thus significantly reduce the effort required for additional insulation against heating up the steel in the event of a fire.
- sheets produced according to the invention have an approx. 0.48 to 0.65. 15% lower yield point ratio than conventional steels that have the same high yield point values.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Heat Treatment Of Steel (AREA)
- Heat Treatment Of Sheet Steel (AREA)
- Chemical Treatment Of Metals (AREA)
- Manufacturing Of Steel Electrode Plates (AREA)
Description
Claims (4)
- Verfahren zur Herstellung von Stahl blech mit Dicken bis 15 mm mit einer Streckgrenze Re > 235 N/mm2 und einem Streckgrenzenverhältnis Re/Rm zwischen 0,4 und 0,65 für den Stahlbau, bestehend aus (in Masse-%):gegebenenfalls0,01 bis 0,14 % C,0,20 bis 1,20 % Mn,0,020 bis 0,045 % Allosl,0,70 bis 0,90 % Cr,0,10 bis 0,25 % Mo,0,01 bis 0,05 % V,Rest Eisen und unvermeidbare Verunreinigungen,bis 0,30 % Si,bis 0,008 % N,bis 0,50 % Cu,bis 0,0040 % B,bis 0,0030 % Ca,bis 0,02 % Nb,bis 0,02 % Ti,
dadurch gekennzeichnet, daß der zu Brammen oder Dünnbrammen vergossene Stahl mit einer Anfangstemperatur im Bereich von 1000 °C bis 1350 °C zu Bändern bei Endwalztemperaturen über 850 °C warmgewalzt wird, daß die Bänder anschließend an Luft auf Haspeltemperatur im Bereich von 720 °C bis 780 °C abgekühlt werden und daß das gehaspelte Band dann zu Blechen abgetafelt wird. - Verfahren nach Anspruch 1, dadurch gekennzeichnet, daß die Bleche bei einer Temperatur im Bereich von 880 °C bis 950 °C normalgeglüht werden.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß die Bleche bei Temperaturen im Bereich von 400 bis 700 °C angelassen werden.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß die Endwalztemperatur im Bereich von 850 bis 900 °C liegt.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19856265 | 1998-12-07 | ||
| DE19856265A DE19856265A1 (de) | 1998-12-07 | 1998-12-07 | Verfahren zur Herstellung feuerresistenter Stahlbleche |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1008667A1 EP1008667A1 (de) | 2000-06-14 |
| EP1008667B1 true EP1008667B1 (de) | 2002-07-03 |
Family
ID=7890160
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99123536A Expired - Lifetime EP1008667B1 (de) | 1998-12-07 | 1999-11-26 | Verfahren zur Herstellung feuerresistenter Stahlbleche |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP1008667B1 (de) |
| AT (1) | ATE220123T1 (de) |
| DE (2) | DE19856265A1 (de) |
| DK (1) | DK1008667T3 (de) |
| ES (1) | ES2178865T3 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AU2006336816B2 (en) * | 2006-01-26 | 2011-09-15 | Giovanni Arvedi | Strip of hot rolled micro-alloyed steel for obtaining finished pieces by cold pressing and shearing |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP4673822B2 (ja) | 2006-11-14 | 2011-04-20 | 新日本製鐵株式会社 | 溶接継手部の靱性に優れた耐火鋼材及びその製造方法 |
| CN102400055B (zh) * | 2010-09-07 | 2014-03-12 | 鞍钢股份有限公司 | 一种低成本屈强比可控高强度高韧性钢板及其制造方法 |
| CN112522595B (zh) * | 2019-09-19 | 2022-10-21 | 宝山钢铁股份有限公司 | 高强薄规格耐火耐候钢板/钢带及其生产方法 |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4990196A (en) * | 1988-06-13 | 1991-02-05 | Nippon Steel Corporation | Process for manufacturing building construction steel having excellent fire resistance and low yield ratio |
| IT1242132B (it) * | 1990-08-01 | 1994-02-16 | Ilva Spa | Procedimento per la produzione di un acciaio strutturale resistente al fuoco |
| JP2828755B2 (ja) * | 1990-08-29 | 1998-11-25 | 株式会社神戸製鋼所 | 溶接性の優れた低降伏比80▲kg▼f/▲mm▼▲上2▼級鋼板の製造方法 |
| JPH08143954A (ja) * | 1994-11-17 | 1996-06-04 | Kobe Steel Ltd | 耐溶接割れ性の優れた引張強さ780N/mm2級鋼板の製造方法 |
| DE19724051C1 (de) * | 1997-06-07 | 1999-03-11 | Thyssen Stahl Ag | Grobbleche einer Dicke bis 50 mm aus feuerresistenten nickelfreien Stählen für den Stahlbau und Verfahren zur Herstellung von Grobblech daraus |
| JP3760587B2 (ja) * | 1997-09-16 | 2006-03-29 | Jfeスチール株式会社 | 耐溶融亜鉛めっき割れ性に優れた耐火電縫溶接角鋼管の 製造方法 |
-
1998
- 1998-12-07 DE DE19856265A patent/DE19856265A1/de not_active Withdrawn
-
1999
- 1999-11-26 EP EP99123536A patent/EP1008667B1/de not_active Expired - Lifetime
- 1999-11-26 ES ES99123536T patent/ES2178865T3/es not_active Expired - Lifetime
- 1999-11-26 DE DE59901917T patent/DE59901917D1/de not_active Expired - Lifetime
- 1999-11-26 DK DK99123536T patent/DK1008667T3/da active
- 1999-11-26 AT AT99123536T patent/ATE220123T1/de not_active IP Right Cessation
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AU2006336816B2 (en) * | 2006-01-26 | 2011-09-15 | Giovanni Arvedi | Strip of hot rolled micro-alloyed steel for obtaining finished pieces by cold pressing and shearing |
Also Published As
| Publication number | Publication date |
|---|---|
| ATE220123T1 (de) | 2002-07-15 |
| DE59901917D1 (de) | 2002-08-08 |
| DE19856265A1 (de) | 2000-06-15 |
| DK1008667T3 (da) | 2002-10-14 |
| ES2178865T3 (es) | 2003-01-01 |
| EP1008667A1 (de) | 2000-06-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE10259230B4 (de) | Verfahren zum Herstellen eines Stahlprodukts | |
| EP2855718B1 (de) | Stahlflachprodukt und verfahren zur herstellung eines stahlflachprodukts | |
| EP2690183B1 (de) | Warmgewalztes Stahlflachprodukt und Verfahren zu seiner Herstellung | |
| EP1309734B2 (de) | Höherfester, kaltumformbarer stahl und stahlband oder -blech, verfahren zur herstellung von stahlband und verwendungen eines solchen stahls | |
| EP3504349B1 (de) | Verfahren zur herstellung eines höchstfesten stahlbandes mit verbesserten eigenschaften bei der weiterverarbeitung und ein derartiges stahlband | |
| DE10116636C2 (de) | Verfahren zur Herstellung von AIMn-Bändern oder Blechen | |
| EP3332046B1 (de) | Hochfester aluminiumhaltiger manganstahl, ein verfahren zur herstellung eines stahlflachprodukts aus diesem stahl und hiernach hergestelltes stahlflachprodukt | |
| DE68928336T2 (de) | Verfahren zur Herstellung von Baustählen mit hoher Feuerbeständigkeit und niedrigem Streckgrenzenverhältnis und dadurch hergestellter Baustahl | |
| EP2383353A2 (de) | Höherfester, Mn-haltiger Stahl, Stahlflachprodukt aus einem solchen Stahl und Verfahren zu dessen Herstellung | |
| EP2767601B1 (de) | Kaltgewalztes Stahlflachprodukt für Tiefziehanwendungen und Verfahren zu seiner Herstellung | |
| EP3658307B9 (de) | Blechbauteil, hergestellt durch warmumformen eines stahlflachprodukts und verfahren zu dessen herstellung | |
| EP4208576A1 (de) | Durch warmumformen eines stahlflachprodukts hergestelltes stahlbauteil, stahlflachprodukt und verfahren zur herstellung eines stahlbauteils | |
| EP2840159A1 (de) | Verfahren zum Herstellen eines Stahlbauteils | |
| DE2334974A1 (de) | Aushaertbarer und hochfester stahl fuer kaltgewalztes blech | |
| DE2714712A1 (de) | Nickellegierung und verfahren zu ihrer herstellung | |
| WO2018029305A1 (de) | Verfahren zur herstellung von walzplattierten blechen | |
| DE2133744B2 (de) | Die verwendung eines vollberuhigten stahles fuer gegenstaende aus warmgewalztem band | |
| DE3685824T2 (de) | Rostfreier martensit-stahl mit ausgezeichneter oxydationsbestaendigkeit, verarbeitbarkeit und korrosionsbestaendigkeit sowie herstellungsverfahren. | |
| WO2014125017A1 (de) | Kaltgewalztes stahlflachprodukt für tiefziehanwendungen und verfahren zu seiner herstellung | |
| EP3872206A1 (de) | Verfahren zur herstellung eines nachbehandelten, kaltgewalzten stahlflachprodukts und nachbehandeltes, kaltgewalztes stahlflachprodukt | |
| DE19724051C1 (de) | Grobbleche einer Dicke bis 50 mm aus feuerresistenten nickelfreien Stählen für den Stahlbau und Verfahren zur Herstellung von Grobblech daraus | |
| DE102022121780A1 (de) | Verfahren zur Herstellung eines kaltgewalzten Stahlflachprodukts | |
| EP1008667A1 (de) | Verfahren zur Herstellung feuerresistenter Stahlbleche | |
| EP3469108B1 (de) | Verfahren zur herstellung eines kaltgewalzten stahlbandes mit trip-eigenschften aus einem hochfesten, manganhaltigen stahl | |
| DE69022523T2 (de) | Rostfreie Stähle mit hoher Zähigkeit und Verfahren zu ihrer Herstellung. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20000417 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid |
Free format text: AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 20010806 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: THYSSENKRUPP STAHL AG |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020703 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020703 |
|
| REF | Corresponds to: |
Ref document number: 220123 Country of ref document: AT Date of ref document: 20020715 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 59901917 Country of ref document: DE Date of ref document: 20020808 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20020828 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20021003 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2178865 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D Ref document number: 1008667E Country of ref document: IE |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030601 |
|
| 26N | No opposition filed |
Effective date: 20030404 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20031130 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20031130 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20081121 Year of fee payment: 10 Ref country code: LU Payment date: 20081121 Year of fee payment: 10 Ref country code: DK Payment date: 20081124 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20081106 Year of fee payment: 10 Ref country code: ES Payment date: 20081124 Year of fee payment: 10 Ref country code: AT Payment date: 20081125 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20081120 Year of fee payment: 10 Ref country code: IT Payment date: 20081125 Year of fee payment: 10 Ref country code: CY Payment date: 20081020 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20081120 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20081120 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20090126 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20091124 Year of fee payment: 11 |
|
| BERE | Be: lapsed |
Owner name: *THYSSENKRUPP STAHL A.G. Effective date: 20091130 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20100601 |
|
| EUG | Se: european patent has lapsed | ||
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20091126 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20100730 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091126 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100601 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091130 Ref country code: CY Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091126 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091126 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20110411 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091127 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110330 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59901917 Country of ref document: DE Effective date: 20110601 Ref country code: DE Ref legal event code: R119 Ref document number: 59901917 Country of ref document: DE Effective date: 20110531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091127 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110531 |