EP0347825B1 - Machine de formage, remplissage et scellage pour des produits laitiers - Google Patents
Machine de formage, remplissage et scellage pour des produits laitiers Download PDFInfo
- Publication number
- EP0347825B1 EP0347825B1 EP89111162A EP89111162A EP0347825B1 EP 0347825 B1 EP0347825 B1 EP 0347825B1 EP 89111162 A EP89111162 A EP 89111162A EP 89111162 A EP89111162 A EP 89111162A EP 0347825 B1 EP0347825 B1 EP 0347825B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- tub
- lid
- roll
- roll holder
- machine according
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000007789 sealing Methods 0.000 title claims abstract description 30
- 238000011049 filling Methods 0.000 title claims abstract description 21
- 235000013365 dairy product Nutrition 0.000 title abstract description 4
- 238000007493 shaping process Methods 0.000 title abstract 2
- 239000011888 foil Substances 0.000 claims abstract description 27
- 238000004080 punching Methods 0.000 claims abstract description 5
- 238000005520 cutting process Methods 0.000 claims abstract description 3
- 239000007788 liquid Substances 0.000 claims abstract description 3
- 238000009434 installation Methods 0.000 claims abstract 2
- 239000002985 plastic film Substances 0.000 claims abstract 2
- 229920006255 plastic film Polymers 0.000 claims abstract 2
- 230000001427 coherent effect Effects 0.000 claims description 4
- 238000000465 moulding Methods 0.000 claims description 2
- 230000007547 defect Effects 0.000 claims 1
- 230000003287 optical effect Effects 0.000 claims 1
- 235000011837 pasties Nutrition 0.000 abstract description 2
- 239000010408 film Substances 0.000 description 28
- 235000013399 edible fruits Nutrition 0.000 description 26
- 239000000654 additive Substances 0.000 description 15
- 230000000996 additive effect Effects 0.000 description 12
- 239000013039 cover film Substances 0.000 description 12
- 238000000034 method Methods 0.000 description 6
- 239000000945 filler Substances 0.000 description 3
- 239000004793 Polystyrene Substances 0.000 description 2
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 2
- 229910052782 aluminium Inorganic materials 0.000 description 2
- 239000008267 milk Substances 0.000 description 2
- 235000013336 milk Nutrition 0.000 description 2
- 210000004080 milk Anatomy 0.000 description 2
- 229920002223 polystyrene Polymers 0.000 description 2
- 230000006978 adaptation Effects 0.000 description 1
- 239000002131 composite material Substances 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 239000012793 heat-sealing layer Substances 0.000 description 1
- 239000010410 layer Substances 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 239000000123 paper Substances 0.000 description 1
- 230000000717 retained effect Effects 0.000 description 1
- 238000009420 retrofitting Methods 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 238000003856 thermoforming Methods 0.000 description 1
- 229920001169 thermoplastic Polymers 0.000 description 1
- 239000004416 thermosoftening plastic Substances 0.000 description 1
- 235000013618 yogurt Nutrition 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B7/00—Closing containers or receptacles after filling
- B65B7/16—Closing semi-rigid or rigid containers or receptacles not deformed by, or not taking-up shape of, contents, e.g. boxes or cartons
- B65B7/162—Closing semi-rigid or rigid containers or receptacles not deformed by, or not taking-up shape of, contents, e.g. boxes or cartons by feeding web material to securing means
- B65B7/164—Securing by heat-sealing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
- B65B9/02—Enclosing successive articles, or quantities of material between opposed webs
- B65B9/04—Enclosing successive articles, or quantities of material between opposed webs one or both webs being formed with pockets for the reception of the articles, or of the quantities of material
- B65B9/042—Enclosing successive articles, or quantities of material between opposed webs one or both webs being formed with pockets for the reception of the articles, or of the quantities of material for fluent material
Definitions
- the invention relates to a form, fill and seal machine for liquid to pasty products.
- a form, fill and seal machine for liquid to pasty products.
- Such a machine is known from US-A-3 374 602.
- the invention relates in particular to a molding, filling and sealing machine, in which the cup recesses are made in the thermoplastic deep-drawing process - as in the subject of DE-A-15 11 668.
- the invention is based on the following general facts: modern four-lane filling units which process, for example, fruit yoghurt or fruit or herb curd and which operate according to the principle disclosed in US Pat. No. 3,374,602, have a theoretical filling capacity of up to approximately 20,000 cups of 150 g each per hour. It is a special feature that milk plants use such filling plants to supply large customers (discounters, chain stores) who order a fixed product sorting for an indefinite period of time. For example, with a four-lane A sorting of 25% (one beaker) of fruit curd with fruit additive A, 50% fruit curd (two beaker lanes) with fruit additive B and 25% (one beaker) of fruit curd with fruit additive C can be produced.
- the fruit additive is generally understood as a fruit admixture or as a fruit base.
- the dairy plant uses an individually printed and otherwise customary cover film, the first web of which in the longitudinal direction has identical prints with regard to the fruit additive A, the two middle webs have identical prints with regard to the fruit additive B and the fourth web has finally identical prints with regard to the fruit additive C wear.
- the film itself is made of aluminum with a heat seal layer on the underside.
- the cover film is provided with line markings which are used to produce the repeat between the cover prints and the cup division by means of photo scanning.
- the cover film always has a small undersize in the longitudinal direction, so that if a repeat error occurs, the cover film web can be permanently stretched along a special stretch, which is described in detail in US Pat. No. 3,374,602.
- a length of cover film is stretched by the appropriate correction measure.
- the cover film is pulled over the already filled cups, which are formed from a coherent thermoforming film (in particular made of polystyrene), and sealed onto the cup edges by means of a heat sealing tool.
- the resulting coherent, filled film arrangement then passes through a punching device for the purpose of cup separation. Without any further sorting process, the rows of cups are fed to each carton as they occur on the machine side: a normal 16-pack carton therefore contains 25% of product A, 50% of product B and 25% of product C without an additional sorting process, in the above example to stay.
- Each product group is assigned the relevant group of cups covering the blank, so that for each product group there is a separate magazine slot that receives the blank.
- cover blanks require a separate, subsequent aseptic treatment, both in their manufacture by cutting or punching and in their handling (transport, refilling of the magazine shafts by hand), which is either not required or much easier to handle in the case of rolled goods.
- the four magazine shafts arranged one behind the other in the conveying direction increase the Overall length of the machine.
- each row of cups extending transversely to the conveying direction already contains, as it were, the assortment requested by the customer, which basically does not change due to multiplication. So surrendered and finally four successive rows of cups, the required range of boxes with a total of sixteen cups.
- the object of the invention is to design the known form, fill and seal machine in such a way that product sorting within the existing one Bucket conveyors can be achieved at any time without additional expenditure on expensive lidding film and with a minimum of mechanical changes.
- This object has been achieved in accordance with the features defined in the characterizing part of patent claim 1.
- the previously existing web-wise uniform - otherwise, however, heterogeneously printed - coherent, wide cover film is to a certain extent broken down into single-web strips, each of which runs individually from a separate supply roll.
- Each single-lane cover film created in this way has special guide means.
- a repeat error occurring there can be eliminated separately and independently of the neighboring single-lane cover films.
- Particularly advantageous in the machine according to the invention is the one-sided arrangement of the supply rolls on the associated roll holder axes, so that the inventive rolls single lane rolls of lid film can be added or replaced in a very short time, ie put on one side.
- the filling unit according to the invention allows rapid, flexible lid-side adaptation to a changed product range without loss of expensive lid film, since only the corresponding individual rolls need to be selected and used in accordance with the desired product sorting.
- a cup filler a so-called form, fill and seal machine
- the feed or conveying direction of the machine is designated by x.
- the cup film 11 made of polystyrene is withdrawn from a supply roll 12 in cycles and then deformed in a thermal deep-drawing device 13 so that cups or cup depressions 14 are formed. Despite its deformation, the overall context of the film 11 is retained.
- each row of cups B r accordingly contains four cup-shaped depressions or cups 14.
- the form, fill and seal machine 10 works intermittently in time.
- three cup rows B r thus a total of twelve cups 14, are formed at the same time in four cup webs B1 - B4.
- the feed division thus comprises three rows of cups B r , so that the filling and metering device 15 has four filling pipe tracks aligned with the cup tracks B 1 - B4, of which only the filling pipe track F 1 with the individual filling pipes 16 can be seen in FIG. 1.
- each of the four filler pipe tracks including the filler pipe track F 1, is acted upon with an individual product mixture.
- the Grerohrbahn F1 fills a fruit curd A, for example, which contains a special fruit additive.
- the other three filling tube tracks are loaded with fruit quark varieties, the fruit additives of which are different from one another.
- the cups 14 filled with fruit curd are closed by means of different cover sealing foils D 1 - D 4, by a heat sealing tool 18, the cover sealing foils provided on the underside with a heat sealing layer on the upper flange-like Presses the edges of the cup 14 and seals it there.
- the film arrangement 11, D 1 - D 4 filled with four different products per cup row B r arrives in a punching device 37, in which twelve filled and closed individual cups 14 A are produced with a punch stroke from a twelve-part cup composite.
- the lid sealing films D1 - D4 lose their integral connection in the longitudinal direction.
- Four individual rows of cups B r of individual cups 14A are accommodated in a carton K. Since each cup row B r of the four-lane form, fill and seal machine contains a fruit curd with different fruit additives, the carton K containing four cup rows B r with its individual cups 14A also has this basic sorting.
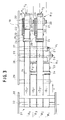
- FIGS. 2 and 3 can be seen in detail how the supply of the separate lid sealing films D1 - D4 takes place.
- a holding plate 19 Above the side next to the conveyor plane E extends in a vertical arrangement, a holding plate 19 to which four mutually separate roller holders R1 - R4 are attached.
- Each roll holder R1 - R4 carries a supply roll V1 - V4.
- Each supply roll V1 - V4 is mounted on a roll holder axis 20, expediently including bearing rolls 21.
- the roller holder axes 20 run parallel to one another and protrude orthogonally from the main plane of extent of the fastening plate 19.
- the storage of the supply rolls V1 - V4 is designed so that they are plugged in from one side in the direction of the mounting plate 19, axially fixed on the arrangement 20, 21 in an unspecified manner and, if necessary, can also be adjusted axially. If an empty or an unneeded supply roll V1 - V soup is to be removed, this is done in a reverse manner away from the mounting plate 19.
- each lid sealing film D1 - D4 initially runs over an end of a guide arm 22 deflection roller 23 and from there via a feeler roller 24, which is rotatably mounted on the end of a roll arm axis 20 according to the double arrow u up and down separate holding arm 25.
- each lid sealing film D1 - D4 is guided with a certain minimum web tension becomes.
- the respective holding arm 25 pivots downward and actuates a brake 26 in a manner not shown, which brakes the process of the supply roll V1-V4 in question while reducing the loop length in order to keep the web tension constant.
- the lid sealing films D2, D4 are then each jointly guided together via freely projecting, continuous, unilaterally rotatably mounted round profile guide axes 27, 28 and the two lid sealing films D1, D3 via the same round profile guide axis 29.
- All cover sealing foils D1 - D4 are then jointly guided beneath both ends of a continuous round profile guide shaft 30, which is pivoted at both ends, to a stretching path or stretching device designated overall by 31.
- the stretching path 31, which forms part of the lid sealing film guideways from the respective supply roll V1 - V4 to the closing device 17, comprises an upper and a lower rotating guide axis 32, 33, both of which are rotatably mounted on both ends. All lid sealing foil webs D1 - D4 are therefore common over the two axes 32, 33 directed. Every single management axis 32, 33 but are assigned to each jaw D1 - D4 a jaw 34, 35 (eight jaws in total).
- Each cover sealing film web D1 - D4 is separately assigned a pivotable eccentric disk 36 in the stretching section 31 in accordance with the double arrow a.
- Each cover sealing film web D1 - D4 in the stretching section 31 is assigned a photo scanner P1 - P4.
- Each sealing film D1 - D4 has inherently a small undersize. As soon as a repeat error occurs, that is, as soon as a lid imprint is not exactly aligned with the associated opening of a cup 14, the relevant lid sealing film web D 1 - D 1 can be individually extended by permanent elongation and the repeat error can thereby be eliminated. The repetition error is eliminated during the cycle-related downtime.
- Each lid sealing film D1 - D4 is provided at certain intervals with edge markings, which can be scanned by the photo scanner P1 -P4. If a repeat error occurs, the respective photo scanner recognizes this by changing the relative position of a marking line. The relevant photo scanner P1 - P be Economics then generates an electrical signal.
- the entire supply roll holder with the essential guide means is thanks to the Common mounting plate 19 designed to a certain extent as a complete add-on unit, which accommodates retrofitting of existing form, fill and seal machines.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Formation And Processing Of Food Products (AREA)
- Dairy Products (AREA)
- Closing Of Containers (AREA)
Claims (12)
- Machine de formage, de remplissage et de fermeture, pour des produits liquides à pâteux, comportant un mmécanisme de remplissage destiné à remplir des cavités en forme de godets (14), façonnées à partir d'une feuille en matière synthétique, de la feuille à godets (11), obtenus par étirage profond, restés accrochés ensemble après la déformation par étirage profond et disposés parallèlement à la direction de transport (x) des godets, en formant plusieurs bandes de godets (B₁ à b₄), et transversalement par rapport à la direction de transport (x), en plusieurs rangées de godets (Br) et fermés, après leur remplissage, par groupes, de façon adhésive, dans un dispositif de fermeture (17), au moyen d'au moins une feuille à couvercles (D₁ à D₄) constituant un ensemble et extraite d'un rouleau de stockage (V₁ à V₄) disposé sur un porte-rouleau (R₁ à R₄), à la suite de quoi les cavités en forme de godets (14) sont séparées au moyen d'un dispositif d'estampage ou de découpage (37), en donnant des godets individuels (14A), puis emballées, la feuille à couvercles (D₁ à D₄) étant pourvue d'impressions de couvercles individuels, adaptées à la taille des godets, identiques les unes aux autres dans chaque bande de godets (B₁ à B₄) et où, entre le porte-rouleau (R₁ à R₄) et le dispositif de fermeture (17), une zone longitudinale de la bande de guidage de feuille à couvercles forme un tronçon d'étirage (31), sur lequel la mise en coïncidence des dessins peut être effectuée, entre l'opération d'application par pression de couvercles individuels et l'opération de division des godets, pendant un temps d'arrêt du transport cadencé de la feuille, caractérisée en ce que la feuille à couvercles est subdivisée en rubans de feuille à couvercles (D₁ à D₄) séparés et monobande, en ce que les rubans de feuille à couvercles (D₁ à D₄) présentent individuellement des impressions de couvercles individuels différentes, en ce qu'à chaque bande de godets (B₁ à B₄) de la feuille à godets (11) encore assemblée est associée un ruban de feuille à couvercles (D₁ à D₄), en ce que chaque ruban de feuille à couvercles (D₁ à D₄) forme un rouleau de stockage (V₁ à V₄) séparé, sur un porte-rouleau (R₁ à R₄) respectif, en ce qu'à chaque ruban de feuille à couvercles (D₁ à D₄) sont associés, sur sa trajectoire de guidage allant du rouleau de stockage (V₁ à V₄) au dispositif de fermeture (17), des moyens de guidage (23, 24; 27 à 30; 31) séparés et en ce que chaque ruban de feuille à couvercles (D₁ à D₄) forme un tronçon d'étirage (31) fonctionnellement indépendant d'erreurs dans la mise en coïncidence des dessins des autres rubans de feuille à couvercles (D₁ à D₄).
- Machine selon la revendication 1,
caractérisée en ce que, dans chaque bande d'étirage (31), après exploration optique (en P₁ à P₄) des marquages de feuille, pour établir la mise en coïncidence de la répétition des dessins, entre l'opération d'application par pression de couvercles et l'opération de division des godets, la feuille à couvercles (D₁ à D₄) est soumise, si elle présente une longueur insuffisante, à une extension longitudinale permanente, entre deux points de serrage, au moyen d'une déformation transversale (en 36). - Machine selon la revendication 1,
caractérisée en ce que chaque porte-rouleau (R₁ à R₄) présente un rouleau palpeur (24), enlacé par une bouche de feuille à couvercles (S), relié fonctionellement, en vue d'assurer ue régulation de la longueur de la bouche, à un frein (26), à l'aide duquel un rouleau de stockage (V₁ à V₄) porté sur l'axe (20) du porte-rouleau correspondant est susceptible d'être freiné. - Machine selon la revendication 3,
caractérisée en ce que le rouleau palpeur (24) est monté rotatif à une extrémité d'un bras support (25), constituant un levier à un bras et actionnant le frein (26) au voisinage de sa zone de palier coaxiale par rapport à l'axe (20) du porte-rouleau. - Machine selon l'une des revendications 1, 3 et 4,
caractérisée en ce que les axes (20) des porte-rouleaux (R₁ à R₄) sont disposés les uns à côté des autres. - Machine selon la revendication 5,
caractérisée en ce que chaque porte-rouleau (R₁ à R₄) présente un axe (20) fixé seulement d'un côté sur un organe de fixation (19) et sur lequel chaque rouleau de stockage (V₁ à V₄) est disposé fou, en pouvant être enfilé d'un côté. - Machine selon la revendication 6,
caractérisée en ce que tous les axes (20) de porte-rouleaux sont parallèles entre eux. - Machine selon la revendication 7,
caractérisée en ce que les axes de porte-rouleaux sont disposés en échelons, transversalement par rapport à la direction de transport (x) des godets et en ce que chaque rouleau de stockage (V₁ à V₄) et la zone, s'étendant sur la bande de guidage de la feuille à couvercles à sceller (entre V₁ à V₄ et 17) de la feuille à couvercles (D₁ à D₄), sont alignés par rapport à la bande de godets (B₁ à B₄) associée. - Machine selon la revendication 7 ou 8,
caractérisée en ce que les axes (20) des porte-rouleaux sont disposés en échelons dans la direction de transport (x) des godets. - Machine selon l'une des revendications 7 à 9,
caractérisée en ce que les axes (20) des porte-rouleaux sont disposés au-dessus du plan de transport (E) des godets, à des niveaux différents. - Machine selon l'une des revendications 1 et 3 à 10,
caractérisée en ce que chaque rouleau de stockage (V₁ à V₄) est disposé réglable en direction axiale, sur son axe (20) de porte-rouleau associé. - Machine selon l'une des revendications 1, 3 à 10,
caractérisée en ce que tous les porte-rouleaux (R₁ à R₄) sont fixés sur une plaque (19) plane, formant un organe de fixation commun, les axes (20) des porte-rouleaux faisant saillie orthogonalement du plan de la plaque, qui est vertical.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT89111162T ATE93464T1 (de) | 1988-06-21 | 1989-06-20 | Form-, fuell- und verschliessmaschine fuer molkereiprodukte. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3820863A DE3820863A1 (de) | 1988-06-21 | 1988-06-21 | Form-, fuell- und verschliessmaschine fuer molkereiprodukte |
| DE3820863 | 1988-06-21 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0347825A1 EP0347825A1 (fr) | 1989-12-27 |
| EP0347825B1 true EP0347825B1 (fr) | 1993-08-25 |
Family
ID=6356887
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89111162A Expired - Lifetime EP0347825B1 (fr) | 1988-06-21 | 1989-06-20 | Machine de formage, remplissage et scellage pour des produits laitiers |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0347825B1 (fr) |
| AT (1) | ATE93464T1 (fr) |
| DE (2) | DE3820863A1 (fr) |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0556526B1 (fr) * | 1992-02-21 | 1994-06-08 | Cofradec S.A. | Récipients recyclables, procédé de leur fabrication, et opercule de fermeture |
| DE4332810A1 (de) * | 1993-09-27 | 1995-03-30 | Focke & Co | Verpackungsmaschine für die Fertigung von Zigaretten-Packungen |
| ITMO20040151A1 (it) | 2004-06-17 | 2004-09-17 | Evifill S R L | Metodo ed impianto per la fabbricazione di confezioni di prodotti |
| IT1396660B1 (it) * | 2009-11-04 | 2012-12-14 | Sarong Spa | Apparato e metodo di saldatura |
| CN107030777B (zh) * | 2017-05-04 | 2018-09-18 | 格来纳塑料科技(苏州)有限公司 | 一种全自动的塑料杯冲孔设备 |
| CN109775002A (zh) * | 2019-03-12 | 2019-05-21 | 温州职业技术学院 | 一种双端封往复式高速枕包机及其包装工艺 |
| CN112550843B (zh) * | 2020-11-19 | 2022-06-14 | 江门市艾可食品有限公司 | 一种饮料生产用自动灌装封塑设备 |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3374602A (en) * | 1965-08-18 | 1968-03-26 | Mahaffy & Harder Eng Co | Indicia registration method and apparatus |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2530306A (en) * | 1945-10-06 | 1950-11-14 | Polaroid Corp | Process and apparatus for forming liquid-carrying containers |
| US2971305A (en) * | 1958-09-08 | 1961-02-14 | Webwraps Inc | Packaging machine |
| GB961294A (en) * | 1960-03-17 | 1964-06-17 | Rose Brothers Ltd | Improvements in web-feeding mechanisms |
| US3296906A (en) * | 1964-09-29 | 1967-01-10 | Beloit Eastern Corp | Wrapper feed for roll wrapper |
| CH436098A (fr) * | 1966-04-19 | 1967-05-15 | Kustner Freres Cie Sa | Procédé de conditionnement de produits solides, pâteux, liquides ou gazeux en alvéoles de matière thermoplastique et machine pour la mise en oeuvre de ce procédé |
| US3908342A (en) * | 1973-10-26 | 1975-09-30 | Fmc Corp | Heat sealing machine |
| FI58465C (fi) * | 1979-10-19 | 1981-02-10 | Waertsilae Oy Ab | System foer frammatning av foerpackningsomslag pao stora pappersrullar |
| DE3605864C1 (de) * | 1986-02-24 | 1987-06-19 | Hassia Verpackung Ag | Verpackungsmaschine mit Folienbanddurchlauf zum kontinuierlich taktweisen Ausformen,Fuellen,Verschliessen und mindestens gruppenweisen Vereinzeln von Bechern |
-
1988
- 1988-06-21 DE DE3820863A patent/DE3820863A1/de not_active Withdrawn
-
1989
- 1989-06-20 AT AT89111162T patent/ATE93464T1/de not_active IP Right Cessation
- 1989-06-20 DE DE89111162T patent/DE58905367D1/de not_active Expired - Fee Related
- 1989-06-20 EP EP89111162A patent/EP0347825B1/fr not_active Expired - Lifetime
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3374602A (en) * | 1965-08-18 | 1968-03-26 | Mahaffy & Harder Eng Co | Indicia registration method and apparatus |
Also Published As
| Publication number | Publication date |
|---|---|
| ATE93464T1 (de) | 1993-09-15 |
| DE3820863A1 (de) | 1989-12-28 |
| DE58905367D1 (de) | 1993-09-30 |
| EP0347825A1 (fr) | 1989-12-27 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE19824797B4 (de) | Beutelherstellungsvorrichtung und Verfahren zum Herstellen von Folienbeutel | |
| EP2163482B1 (fr) | Procédé et dispositif destinés à la fabrication de fûts | |
| EP2415590B1 (fr) | Dispositif de fabrication de sachets de tabac | |
| EP1437202B1 (fr) | Dispositif et procédé pour la séparation de poses dans une machine pour la production d'éléments plans découpés à partir d'une bande | |
| DE69433887T2 (de) | Verpackungssystem und verpackungsverfahren | |
| EP2336037B1 (fr) | Dispositif et procédé d'emballage par groupes d'objets | |
| DD296641A5 (de) | On-line-praegevorrichtung fuer beschriftungsmaschinen | |
| WO2019219967A1 (fr) | Procédé de commande de la position du bord de bande de produits | |
| CH677338A5 (fr) | ||
| EP2076443A1 (fr) | Machine d'emballage avec un dispositif d'étiquetage | |
| DE69805885T2 (de) | Vorrichtung zum Verpacken von Getränkebehältern mittels Heiss-Schrumpfbarer Folie | |
| EP0347825A1 (fr) | Machine de formage, remplissage et scellage pour des produits laitiers | |
| DE2731023B2 (de) | Verfahren und Vorrichtung zum Zuschneiden von Bögen zu Einzelblättern und zum geordneten Stapeln der Einzelblätter | |
| DE19610900A1 (de) | Falzapparat mit einem heftebildenden Zusatzmodul | |
| EP3966111B1 (fr) | Machine d'emballage sans danseurs | |
| EP3994088A1 (fr) | Machine à poinçonner dotée d'un système de transport sous forme d'un système de pinces à chaîne, et procédé d'ouverture d'au moins un élément de retenue | |
| DE4127854A1 (de) | Vorrichtung zum zufuehren von plattenfoermigen zuschnitten zu einer tiefziehmaschine | |
| EP4003890B1 (fr) | Machine de traitement de feuilles avec au moins un dispositif de stockage de feuilles, et procédé de stockage de feuilles | |
| EP3077306B1 (fr) | Dispositif et procédé de découpage d'un matériau en bande en bandes partielles et d'écartement des bandes partielles | |
| EP0014858A1 (fr) | Procédé et dispositif pour appliquer des rubans d'ouverture ou analogues sur une feuille de matériau d'empaquetage | |
| WO2005058563A1 (fr) | Decoupeur longitudinal a lame deplaçable verticalement et cylindre antagoniste | |
| DE10300233B3 (de) | Vorrichtung und Verfahren zur Ablage von aus einer Materialbahn ausgeschnittenen Flachmaterialstücken | |
| DE20118881U1 (de) | Vorrichtung zur Herstellung von Verpackungen aus tiefgezogenen Folien | |
| DE2200280B2 (de) | Bahnförmiges Verpackungsmaterial und Verfahren zu dessen Herstellung | |
| DE102019128981B4 (de) | Bogenbearbeitungsmaschine mit einem als Kettengreifersystem ausgebildeten Transportsystem und ein Verfahren zum Verstellen eines Kettengreiferöffners |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE FR GB IT LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19900615 |
|
| 17Q | First examination report despatched |
Effective date: 19910911 |
|
| RAP3 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: MILCHWERKE KOELN/WUPPERTAL EG |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE FR GB IT LI LU NL SE |
|
| REF | Corresponds to: |
Ref document number: 93464 Country of ref document: AT Date of ref document: 19930915 Kind code of ref document: T |
|
| ET | Fr: translation filed | ||
| REF | Corresponds to: |
Ref document number: 58905367 Country of ref document: DE Date of ref document: 19930930 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19930920 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| EPTA | Lu: last paid annual fee | ||
| 26N | No opposition filed | ||
| EAL | Se: european patent in force in sweden |
Ref document number: 89111162.7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19980611 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19980624 Year of fee payment: 10 Ref country code: BE Payment date: 19980624 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19980625 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19980626 Year of fee payment: 10 Ref country code: AT Payment date: 19980626 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19980630 Year of fee payment: 10 Ref country code: NL Payment date: 19980630 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 19980728 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP |
|
| NLS | Nl: assignments of ep-patents |
Owner name: TUFFI CAMPINA MILCHWERKE GMBH & CO. KG |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PUE Owner name: MILCHWERKE KOELN/WUPPERTAL EG TRANSFER- TUFFI CAMP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990620 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990620 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990620 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19990629 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990630 Ref country code: FR Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19990630 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990630 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990630 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E |
|
| BERE | Be: lapsed |
Owner name: TUFFI CAMPINA MILCHWERKE G.M.B.H. & CO. K.G. Effective date: 19990630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20000101 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19990620 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| EUG | Se: european patent has lapsed |
Ref document number: 89111162.7 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20000101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20000503 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050620 |