CN115194929A - Full-automatic building block forming production line and production process thereof - Google Patents
Full-automatic building block forming production line and production process thereof Download PDFInfo
- Publication number
- CN115194929A CN115194929A CN202210739861.6A CN202210739861A CN115194929A CN 115194929 A CN115194929 A CN 115194929A CN 202210739861 A CN202210739861 A CN 202210739861A CN 115194929 A CN115194929 A CN 115194929A
- Authority
- CN
- China
- Prior art keywords
- frame
- brick
- synchronous
- die
- rack
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images






Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B15/00—General arrangement or layout of plant ; Industrial outlines or plant installations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B13/00—Feeding the unshaped material to moulds or apparatus for producing shaped articles; Discharging shaped articles from such moulds or apparatus
- B28B13/04—Discharging the shaped articles
- B28B13/06—Removing the shaped articles from moulds
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B3/00—Producing shaped articles from the material by using presses; Presses specially adapted therefor
- B28B3/02—Producing shaped articles from the material by using presses; Presses specially adapted therefor wherein a ram exerts pressure on the material in a moulding space; Ram heads of special form
- B28B3/022—Producing shaped articles from the material by using presses; Presses specially adapted therefor wherein a ram exerts pressure on the material in a moulding space; Ram heads of special form combined with vibrating or jolting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65G—TRANSPORT OR STORAGE DEVICES, e.g. CONVEYORS FOR LOADING OR TIPPING, SHOP CONVEYOR SYSTEMS OR PNEUMATIC TUBE CONVEYORS
- B65G61/00—Use of pick-up or transfer devices or of manipulators for stacking or de-stacking articles not otherwise provided for
Landscapes
- Engineering & Computer Science (AREA)
- Ceramic Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Devices For Post-Treatments, Processing, Supply, Discharge, And Other Processes (AREA)
Abstract
本发明涉及一种全自动砌块成型生产线及其生产工艺,该全自动砌块成型生产线包括免托板制砖成型机和砌砖成品输送机,所述免托板制砖成型机包括滑动设置在成型机架上的料车装置,所述料车装置的上方设置有可横移的料斗,所述料车装置的前方设置有压模成型装置,所述压模成型装置的正下方设置有振动装置,所述压模成型装置和振动装置之间设置有减震装置,所述压模成型装置的顶部设置有同步脱模装置。该全自动砌块成型生产线机械化程度高、劳动强度低、产品质量好。

The invention relates to a full-automatic block forming production line and a production process thereof. The full-automatic block forming production line comprises a pallet-free brick making machine and a brick-laying finished product conveyor, and the pallet-free brick making machine includes a sliding arrangement On the feeder device on the forming frame, a hopper that can be moved laterally is arranged above the feeder device, a compression molding device is arranged in front of the feeder device, and a compression molding device is arranged directly below the compression molding device. A vibration device, a shock absorption device is arranged between the compression molding device and the vibration device, and a synchronous demoulding device is arranged on the top of the compression molding device. The fully automatic block forming production line has high degree of mechanization, low labor intensity and good product quality.
Description
技术领域technical field
本发明具体涉及一种全自动砌块成型生产线及其生产工艺。The invention specifically relates to a fully automatic block forming production line and a production process thereof.
背景技术Background technique
随着我国墙体材料改革的深入发展,发展一种生产效率高且质量好的新型墙体材料已经是必然的趋势。各种混泥土建筑砌块的生产都是将搅拌好的混泥土放到专用模具中经过压实后,再脱模晾干而成。采用人工生产,不仅劳动强度大,生产效率非常低下,由于很难做到统一的震动和压实效果,产品的质量也得不到保障,且压头会由于压差以及左右装配间隙不均导致两侧压头及脱模不能同步顺畅动作,十分影响产品的成品度及质量,且生产后的砖经过养护后要卖出去,平常都是靠人工一块一块的把砖搬到车上再运输出去,运输效率低下,且十分浪费人力资源。With the in-depth development of wall material reform in China, it is an inevitable trend to develop a new type of wall material with high production efficiency and good quality. The production of various concrete building blocks is made by placing the mixed concrete in a special mold, compacting it, and then demoulding it and drying it. The use of manual production is not only labor-intensive, but also very low in production efficiency. Because it is difficult to achieve uniform vibration and compaction effects, the quality of the product cannot be guaranteed, and the indenter will be caused by the pressure difference and uneven assembly gap between the left and right. The indenters on both sides and the demoulding cannot move smoothly and synchronously, which greatly affects the finished product and quality of the product, and the produced bricks need to be sold after curing. Usually, the bricks are moved to the car one by one manually and then transported. Going out, transportation is inefficient, and it is a waste of human resources.
发明内容SUMMARY OF THE INVENTION
鉴于现有技术的不足,本发明所要解决的技术问题是提供一种全自动砌块成型生产线及其生产工艺。In view of the deficiencies of the prior art, the technical problem to be solved by the present invention is to provide a fully automatic block forming production line and a production process thereof.
为解决上述技术问题,本发明采用的技术方案是:一种全自动砌块成型生产线,包括免托板制砖成型机和砌砖成品输送机,所述免托板制砖成型机包括滑动设置在成型机架上的料车装置,所述料车装置的上方设置有可横移的料斗,所述料车装置的前方设置有压模成型装置,所述压模成型装置的正下方设置有振动装置,所述压模成型装置和振动装置之间设置有减震装置,所述压模成型装置的顶部设置有同步脱模装置。In order to solve the above technical problems, the technical solution adopted in the present invention is: a fully automatic block forming production line, including a pallet-free brick making machine and a brick-laying finished product conveyor, and the pallet-free brick making machine includes a sliding setting On the feeder device on the forming frame, a hopper that can be moved laterally is provided above the feeder device, a compression molding device is provided in front of the feeder device, and a compression molding device is provided directly below the compression molding device. A vibration device, a shock absorption device is arranged between the compression molding device and the vibration device, and a synchronous demoulding device is arranged on the top of the compression molding device.
在进一步的,所述压模成型装置包括压模机架、压模油缸、上压架、上模框和下模框,所述压模机架的两侧底部和顶部分别设置有套座,相同一侧的两竖直对齐套座之间活动设置有一导柱,多个所述导柱的顶部之间固定有所述同步脱模装置,所述压模油缸的缸体固定在压模机架的顶部,所述压模油缸的活塞端朝下,所述上压架固定安装在所述压模油缸的活塞端,所述上压架的两侧端滑动分别套设在两侧的导柱上,所述上模框固定安装在所述上压架的底部,所述上模框的底部设置有多个上压头,所述下模框位于上压头的正下方,所述下模框的两侧端固定安装在两侧的导柱上。Further, the compression molding device includes a compression molding frame, a compression molding oil cylinder, an upper compression frame, an upper mold frame and a lower mold frame, and the bottom and top of both sides of the compression molding frame are respectively provided with sleeves, A guide post is movably arranged between the two vertically aligned sleeves on the same side, the synchronous demolding device is fixed between the tops of the plurality of guide posts, and the cylinder body of the compression molding oil cylinder is fixed on the compression molding machine. The top of the frame, the piston end of the die cylinder faces downward, the upper press frame is fixedly mounted on the piston end of the die press cylinder, and the two sides of the upper press frame slide with guide rails respectively sleeved on both sides. On the column, the upper die frame is fixedly mounted on the bottom of the upper pressing frame, the bottom of the upper die frame is provided with a plurality of upper pressing heads, the lower die frame is located directly below the upper pressing head, and the lower Both sides of the mold frame are fixedly installed on the guide posts on both sides.
在进一步的,所述同步脱模装置包括同步架、两个同步连杆、两个脱模油缸和同步轴,所述同步架固定在多个所述导柱的顶部之间,所述同步架的中间顶部安装有同步台,所述脱模油缸的缸体固定在压模机架的顶部,所述脱模油缸的活塞端朝上固定在所述同步台上,所述同步轴转动安装在压模机架的顶部有一侧,所述同步连杆的一端转动安装在同步轴上,所述同步连杆的另一端铰接有一同步臂,所述同步臂的另一端转动安装在同步台的顶部。Further, the synchronous demolding device includes a synchronous frame, two synchronous connecting rods, two demolding oil cylinders and a synchronous shaft, the synchronous frame is fixed between the tops of the plurality of the guide posts, and the synchronous frame A synchronization table is installed on the top of the middle of the mold release cylinder, the cylinder body of the demoulding oil cylinder is fixed on the top of the die frame, the piston end of the mold release oil cylinder is upwardly fixed on the synchronization table, and the synchronization shaft is rotatably installed on the The top of the die frame has one side, one end of the synchronizing link is rotatably mounted on the synchronizing shaft, the other end of the synchronizing link is hinged with a synchronizing arm, and the other end of the synchronizing arm is rotatably mounted on the top of the synchronizing table .
在进一步的,所述下模框的两侧通过一锁紧块固定安装在导柱上,所述锁紧块的顶部安装有锥套组件,所述锥套组件锁紧在所述导柱上,所述锥套组件包括锥形外套和锥形内套,所述导柱上开设有第一环形凹槽,所述锥形内套的内缘端嵌入所述第一环形凹槽内,所述锥形外套套设在所述导柱上,所述锥形外套的内圈开设有锥形环槽,所述锥形内套的外缘端嵌入所述锥形环槽内,所述锥形外套的底部和锁紧块之间通过螺栓固定连接。Further, both sides of the lower mold frame are fixedly mounted on the guide post through a locking block, a taper sleeve assembly is installed on the top of the locking block, and the taper sleeve assembly is locked on the guide post , the conical sleeve assembly includes a conical outer sleeve and a conical inner sleeve, the guide post is provided with a first annular groove, and the inner edge end of the conical inner sleeve is embedded in the first annular groove, so The conical outer sleeve is sleeved on the guide post, the inner ring of the conical outer sleeve is provided with a conical annular groove, the outer edge end of the conical inner sleeve is embedded in the conical annular groove, the cone The bottom of the outer casing and the locking block are fixedly connected by bolts.
在进一步的,所述振动装置包括振动基座,所述振动基座安装在压模机架的底部,所述振动基座内设置有振动电机,所述振动基座的顶部安装有多个传动振动头。Further, the vibration device includes a vibration base, the vibration base is installed at the bottom of the die frame, a vibration motor is arranged in the vibration base, and a plurality of transmissions are installed on the top of the vibration base vibrating head.
在进一步的,所述减震装置包括减震框,所述减震框安装在压模机架上,所述减震框和压模机架之间形成有用于容纳锁紧块的减震槽,所述减震槽的底部安装有减震弹簧。Further, the shock absorbing device includes a shock absorbing frame, the shock absorbing frame is mounted on the die frame, and a shock absorbing groove for accommodating the locking block is formed between the shock absorbing frame and the die frame. , a shock-absorbing spring is installed at the bottom of the shock-absorbing groove.
在进一步的,所述砌砖成品输送机包括沿砌砖输送方向顺序设置的进砖输送线、升板设备、过渡输送线和码垛主设备,所述码垛主设备的一侧设置收板设备,所述码垛主设备的输入端架设在过渡输送线的输出端与收板设备的输入端之间,所述过渡输送线的输出端与收板设备的输入端连接。Further, the brick-laying finished product conveyor includes a brick-feeding conveying line, a plate-lifting device, a transition conveying line and a stacking main device sequentially arranged along the brick-laying conveying direction, and a closing plate is arranged on one side of the main stacking device. equipment, the input end of the main stacking equipment is erected between the output end of the transitional conveying line and the input end of the plate-receiving device, and the output end of the transitional conveying line is connected to the input end of the plate-receiving device.
在进一步的,所述码垛主设备包括码垛机架、第一推头组件、固定板、第二推头组件、抽板和托盘,所述第一推头组件安装在码垛机架的输入端一侧,所述固定板安装在码垛机架的中部,所述抽板可横移地安装在码垛机架上,所述抽板的输入端位于固定板输出端的一侧,所述第二推头组件安装在码垛机架的中部并位于抽板的上方,所述托盘通过升降机构可升降地设置在码垛机架的输出端一侧,所述码垛机架位于托盘上方分别设置有用于夹住砖层的前推头、左推头和右推头,所述前推头位于第二推头组件的前方,所述前推头、左推头和右推头均由气缸控制。Further, the stacking main equipment includes a stacking frame, a first pusher assembly, a fixing plate, a second pusher assembly, a drawing plate and a tray, and the first pusher assembly is installed on the stacking frame. On one side of the input end, the fixed plate is installed in the middle of the palletizing frame, the drawing plate can be installed on the palletizing frame traversely, and the input end of the drawing plate is located on the side of the output end of the fixed plate, so The second push head assembly is installed in the middle of the stacking frame and is located above the drawer, the tray can be lifted and lowered by the lifting mechanism and is arranged on the side of the output end of the stacking frame, and the stacking frame is located on the tray. The upper part is respectively provided with a front push head, a left push head and a right push head for clamping the brick layer, the front push head is located in front of the second push head assembly, the front push head, the left push head and the right push head are all Controlled by the cylinder.
在进一步的,所述第一推头组件包括第一推头电机、第一推板、第一推板气缸和第一推车架,所述第一推车架可横移地安装在码垛机架上,所述第一推车架上转动安装有第一推车转轴,所述第一推头电机安装在第一推车架上用以驱动第一推车转轴转动,所述第一推车转轴的两端安装有第一滚轮,所述码垛机架的顶部安装有供第一滚轮转动的推车轨道,所述第一推板气缸安装在第一推车架上,所述第一推板气缸的活塞端朝下设置,所述第一推板安装在第一推板气缸的活塞端,所述第一推板位于第一推车架的前方。Further, the first push head assembly includes a first push head motor, a first push plate, a first push plate cylinder and a first cart frame, the first push frame is movably installed on the pallet On the frame, a first cart rotating shaft is rotatably installed on the first cart frame, and the first push head motor is installed on the first cart frame to drive the first cart rotating shaft to rotate, and the first cart rotating shaft is rotated. The two ends of the trolley shaft are installed with first rollers, the top of the stacking frame is installed with a trolley track for the first roller to rotate, the first push plate cylinder is installed on the first trolley frame, the The piston end of the first push plate cylinder is disposed downward, the first push plate is mounted on the piston end of the first push plate cylinder, and the first push plate is located in front of the first cart frame.
在进一步的,所述第一推板上安装有第一导架,所述第一推车架上竖直设置有与多个第一导架相配合的第一导轮。Further, a first guide frame is installed on the first push plate, and a first guide wheel matched with a plurality of first guide frames is vertically arranged on the first push frame.
在进一步的,所述第二推头组件包括第二推头电机、第二推板、第二推板气缸和第二推车架,所述第二推车架可横移地安装在码垛机架上,所述第二推车架上转动安装有第二推车转轴,所述第二推头电机安装在第二推车架上用以驱动第二推车转轴转动,所述第二推车转轴的两端安装有第二滚轮,所述第二滚轮在推车轨道上转动,所述第二推板气缸安装在第二推车架的后端,所述第二推板气缸的活塞端朝下设置,所述第二推板安装在第二推板气缸的活塞端,所述第二推板位于第二推车架的前方。Further, the second push head assembly includes a second push head motor, a second push plate, a second push plate cylinder and a second cart frame, and the second cart frame is movably installed on the pallet On the frame, a second cart rotating shaft is rotatably installed on the second cart frame, and the second push head motor is installed on the second cart frame to drive the second cart rotating shaft to rotate, the second cart rotating shaft Both ends of the cart rotating shaft are installed with second rollers, the second rollers rotate on the cart track, the second push plate cylinder is installed at the rear end of the second cart frame, and the second push plate cylinder The piston end is arranged downward, the second push plate is mounted on the piston end of the second push plate cylinder, and the second push plate is located in front of the second cart frame.
在进一步的,所述第二推板上安装有第二导架,所述第二推车架上竖直设置有与多个第二导架相配合的第二导轮,所述第二推头组件的后端安装有第三气缸,所述第三气缸的活塞端朝下,所述第三气缸的活塞端设置有隔板架。Further, a second guide frame is installed on the second push plate, and a second guide wheel matched with a plurality of second guide frames is vertically arranged on the second push frame. A third cylinder is installed at the rear end of the head assembly, the piston end of the third cylinder faces downward, and the piston end of the third cylinder is provided with a partition frame.
在进一步的,所述升降机构包括升降电机、升降架、升降链条和升降转轴,所述升降转轴转动安装在码垛机架的顶部,所述升降电机通过一电机架安装在码垛机架的上方,所述升降电机和升降转轴之间通过传动链条传动连接,所述升降转轴上设置有供升降链条套设用的升降齿轮,所述升降架的中间设置有旋转盘,所述升降架的底部设置有控制旋转盘转动的旋转减速电机,所述托盘放置在旋转盘上。Further, the lifting mechanism includes a lifting motor, a lifting frame, a lifting chain and a lifting rotating shaft, the lifting rotating shaft is rotatably installed on the top of the stacking frame, and the lifting motor is installed on the top of the stacking frame through a motor frame. Above, the elevating motor and the elevating rotating shaft are connected by a transmission chain, the elevating rotating shaft is provided with a elevating gear for the elevating chain to be sleeved on, a rotating disk is arranged in the middle of the elevating frame, and the The bottom is provided with a rotary deceleration motor that controls the rotation of the rotary disk, and the tray is placed on the rotary disk.
在进一步的,所述码垛主设备的输出端设置有出砖设备,所述出砖设备包括出砖机架、出砖电机和出砖双轨道输送线,所述出砖机架安装在码垛机架的底部,所述出砖双轨道输送线的双轨道安装出砖机架上并对称分布在旋转盘的两侧,所述出砖电机安装在出砖机架上用以驱动出砖双轨道输送线输送托盘。Further, the output end of the main stacking device is provided with a brick ejecting device, and the brick ejecting device includes a brick ejecting rack, a brick ejecting motor and a brick ejecting double-track conveyor line, and the brick ejecting rack is installed on the pallet. At the bottom of the stacking rack, the double rails of the double-track delivery line for bricks are installed on the bricks rack and are symmetrically distributed on both sides of the rotating disc, and the brick-out motor is installed on the brick-out rack to drive the bricks Double track conveyor line conveys pallets.
在进一步的,所述升板设备包括升板架、夹板机构、链条横移机构和链条升降机构,所述升板架架设在进砖输送线和过渡输送线之间,所述链条横移机构安装在升板架的顶部,所述链条升降机构安装在链条横移机构上,所述夹板机构安装在链条升降机构上。Further, the plate-lifting device includes a plate-lifting frame, a splint mechanism, a chain traverse mechanism and a chain lifting mechanism, the plate-lifting frame is erected between the brick feeding conveyor line and the transition conveyor line, and the chain traverse mechanism It is installed on the top of the lift frame, the chain lift mechanism is installed on the chain traverse mechanism, and the splint mechanism is installed on the chain lift mechanism.
在进一步的,所述收板设备包括入板输送线、升降板机构和出板输送线,所述升降板机构设置在入板输送线输出端和出板输送线输入端之间,所述出板输送线的输入端位于升降板机构的底部,所述升降板机构内设置有可横移升降的抓板码垛机械勾。Further, the board receiving device includes a board input conveyor line, a lifting board mechanism and a board output line, the lifting board mechanism is arranged between the output end of the board input conveyor line and the input end of the board output conveyor line, and the output board The input end of the board conveying line is located at the bottom of the lifting board mechanism, and the lifting board mechanism is provided with a mechanical hook for grabbing and stacking that can be moved horizontally and lifted.
为解决上述技术问题,本发明采用的技术方案是:一种全自动砌块成型生产线的生产工艺,采用上述全自动砌块成型生产线,并包括以下步骤:In order to solve the above-mentioned technical problems, the technical scheme adopted in the present invention is: a production process of a fully automatic block forming production line, which adopts the above-mentioned automatic block forming production line, and comprises the following steps:
S1、料车装置将物料均匀的漏到下模框中,压模油缸控制上压架下降;S1. The feeding truck device evenly leaks the material into the lower die frame, and the die cylinder controls the upper pressing frame to descend;
S2、上压架带动上压头向下压,振动装置同时开始振动,把下模框内的物料压实成型;S2. The upper pressing frame drives the upper pressing head to press down, the vibration device starts to vibrate at the same time, and the material in the lower mold frame is compacted and formed;
S3、随后脱模油缸启动,脱模油缸带动同步架上升;S3. Then the demolding cylinder is started, and the demolding cylinder drives the synchronizing frame to rise;
S4、同步架带动导柱上升,导柱带动锁紧块和下模框一起上升,下模框上升使其与物料分离;S4. The synchronous frame drives the guide column to rise, the guide column drives the locking block and the lower die frame to rise together, and the lower die frame rises to separate it from the material;
S5、制成的砖分层放置到专用托板上进行养护处理;S5. The made bricks are placed in layers on a special pallet for maintenance treatment;
S6、将养护好的砖连托板多层一起通过叉车放置到进砖输送线上;S6. Place the cured bricks together with the multi-layer pallets on the brick feeding conveyor line through a forklift;
S7、由进砖输送线将一层砖与板输送至升板设备上;S7. A layer of bricks and plates are transported to the lifting equipment by the brick feeding conveying line;
S8、由升板设备将砖和板转移至过渡输送线上;S8. The bricks and plates are transferred to the transition conveyor line by the plate lifting equipment;
S9、然后由过渡输送线将砖与板输送至码垛主设备上;S9. Then the bricks and plates are conveyed to the main stacking equipment by the transition conveying line;
S10、板层通过收板设备将其码垛收集起来;S10, the board layers are collected by stacking equipment;
S11、而码垛主设备将进来的砖层码垛完成;S11. The main stacking equipment completes the stacking of the incoming brick layer;
S12、最后通过出砖设备将其输送出去。S12. Finally, the bricks are transported out through the brick producing equipment.
与现有技术相比,本发明具有以下有益效果:该全自动砌块成型生产线通过在压模成型装置的下方设置振动装置,有效提高压模成型的效率,在压模成型装置和振动装置之间设置减震装置,减少设备的损坏程度,并通过压模成型装置上方的同步脱模装置保证砌砖脱模成型的效果,该砌砖成品输送机通过将养护好的砖连托板多层一起通过叉车放置到进砖输送线上,由进砖输送线将一层砖与板输送至升板设备上,由升板设备将砖和板转移至过渡输送线上,然后由过渡输送线将砖与板输送至码垛主设备上,板层通过收板设备将其码垛收集起来,而码垛主设备将进来的砖层码垛完成,最后通过出砖设备将其输送出去,不仅方便且快捷,而且省人工,可大大降低成本,机械化程度高、劳动强度低、产品质量好。Compared with the prior art, the present invention has the following beneficial effects: the fully automatic block forming production line effectively improves the efficiency of the compression molding by arranging the vibration device below the compression molding device, and between the compression molding device and the vibration device A shock absorbing device is installed between the two parts to reduce the damage of the equipment, and the synchronous demoulding device above the compression molding device can ensure the effect of demoulding and forming of bricks. At the same time, they are placed on the brick feeding conveyor line by a forklift. The brick feeding conveyor line transports a layer of bricks and boards to the lifting equipment, and the lifting equipment transfers the bricks and boards to the transition conveyor line. The bricks and boards are transported to the main stacking equipment, the board layers are collected by the stacking equipment, and the main stacking equipment completes the stacking of the incoming brick layers, and finally transports them out through the brick discharging equipment, which is not only convenient It is fast and labor-saving, which can greatly reduce costs. It has high degree of mechanization, low labor intensity and good product quality.
附图说明Description of drawings
图1为本发明实施例的免托板制砖成型机的前视图。FIG. 1 is a front view of a pallet-free brick forming machine according to an embodiment of the present invention.
图2为本发明实施例的免托板制砖成型机的侧视图。FIG. 2 is a side view of the pallet-free brick forming machine according to the embodiment of the present invention.
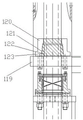
图3为本发明实施例的锥套组件的结构示意图。FIG. 3 is a schematic structural diagram of a taper sleeve assembly according to an embodiment of the present invention.
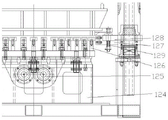
图4为本发明实施例的振动装置的结构示意图。FIG. 4 is a schematic structural diagram of a vibrating device according to an embodiment of the present invention.
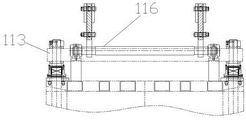
图5为本发明实施例的同步脱模装置的侧视图。FIG. 5 is a side view of a synchronous demoulding device according to an embodiment of the present invention.
图6为本发明实施例的同步脱模装置的前视图。FIG. 6 is a front view of the synchronous demolding device according to the embodiment of the present invention.
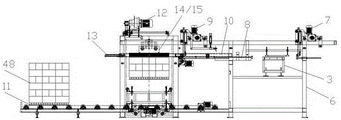
图7为本发明实施例的砌砖成品输送机的结构示意图。FIG. 7 is a schematic structural diagram of a finished brick-laying conveyor according to an embodiment of the present invention.
图8为本发明实施例的码垛主设备的结构示意图。FIG. 8 is a schematic structural diagram of a main palletizing device according to an embodiment of the present invention.
图9为本发明实施例的第一推头组件的结构示意图。FIG. 9 is a schematic structural diagram of a first pusher assembly according to an embodiment of the present invention.
图10为本发明实施例的第二推头组件的结构示意图。FIG. 10 is a schematic structural diagram of a second pusher assembly according to an embodiment of the present invention.
图11为本发明实施例的码垛机架的结构示意图。FIG. 11 is a schematic structural diagram of a palletizing frame according to an embodiment of the present invention.
图12为本发明实施例的出砖设备的结构示意图。FIG. 12 is a schematic structural diagram of a brick producing device according to an embodiment of the present invention.
图中标记:101、压模成型装置;102、振动装置;103、减震装置;104、同步脱模装置;105、压模机架;106、压模油缸;107、上压架;108、上模框;109、下模框;110、套座;111、导柱;112、上压头;113、同步架;114、同步连杆;115、脱模油缸;116、同步轴;117、同步台;118、同步臂;119、锁紧块;120、锥形外套;121、锥形内套;122、第一环形凹槽;123、锥形环槽;124、振动基座;125、振动电机;126、传动振动头;127、减震框;128、减震槽;129、减震弹簧。Marked in the figure: 101, compression molding device; 102, vibration device; 103, shock absorption device; 104, synchronous demoulding device; 105, compression molding frame; 106, compression molding cylinder; 107, upper pressing frame; 108, Upper die frame; 109, lower die frame; 110, sleeve seat; 111, guide post; 112, upper indenter; 113, synchronizing frame; 114, synchronizing connecting rod; 115, demoulding cylinder; 116, synchronizing shaft; 117, 118, synchronizing arm; 119, locking block; 120, conical outer sleeve; 121, conical inner sleeve; 122, first annular groove; 123, conical annular groove; 124, vibration base; 125, Vibration motor; 126, transmission vibrating head; 127, shock-absorbing frame; 128, shock-absorbing groove; 129, shock-absorbing spring.
具体实施方式Detailed ways
为了让本发明的上述特征和优点更明显易懂,下面特举实施例,并配合附图,作详细说明如下。In order to make the above-mentioned features and advantages of the present invention more obvious and easy to understand, the following embodiments are given and described in detail in conjunction with the accompanying drawings.
如图1~12所示,一种全自动砌块成型生产线,包括免托板制砖成型机和砌砖成品输送机,所述免托板制砖成型机包括滑动设置在成型机架上的料车装置,所述料车装置的上方设置有可横移的料斗,所述料车装置的前方设置有压模成型装置101,所述压模成型装置101的正下方设置有振动装置102,所述压模成型装置101和振动装置102之间设置有减震装置103,所述压模成型装置101的顶部设置有同步脱模装置104。As shown in Figures 1 to 12, a fully automatic block forming production line includes a pallet-free brick making machine and a finished brick-laying conveyor. A feeder device, a hopper that can be moved laterally is provided above the feeder device, a
在本实施例中,所述压模成型装置101包括压模机架105、压模油缸106、上压架107、上模框108和下模框109,所述压模机架105的两侧底部和顶部分别设置有套座110,相同一侧的两竖直对齐套座110之间活动设置有一导柱111,多个所述导柱111的顶部之间固定有所述同步脱模装置104,所述压模油缸106的缸体固定在压模机架105的顶部,所述压模油缸106的活塞端朝下,所述上压架107固定安装在所述压模油缸106的活塞端,所述上压架107的两侧端滑动分别套设在两侧的导柱111上,所述上模框108固定安装在所述上压架107的底部,所述上模框108的底部设置有多个上压头112,所述下模框109位于上压头112的正下方,所述下模框109的两侧端固定安装在两侧的导柱111上。In this embodiment, the
在本实施例中,所述同步脱模装置104包括同步架113、两个同步连杆114、两个脱模油缸115和同步轴116,所述同步架113固定在多个所述导柱111的顶部之间,所述同步架113的中间顶部安装有同步台117,所述脱模油缸115的缸体固定在压模机架105的顶部,所述脱模油缸115的活塞端朝上固定在所述同步台117上,所述同步轴116转动安装在压模机架105的顶部有一侧,所述同步连杆114的一端转动安装在同步轴116上,所述同步连杆114的另一端铰接有一同步臂118,所述同步臂118的另一端转动安装在同步台117的顶部,制砖时,当砖成型后要从下模框109脱模,由于左右宽度比较大,两边的脱模油缸115行走不一致,脱模时会造成砖左右出现高度不一样的情况,当脱模油缸115带动同步台117上升,同步台117带动同步机架113上升,通过同步臂118和同步连杆114的配合,转动同步轴116使得两边的脱模油缸115行走一致,砖脱模时就不会出现高度不一致的现象。In this embodiment, the
在本实施例中,所述下模框109的两侧通过一锁紧块119固定安装在导柱111上,所述锁紧块119的顶部安装有锥套组件,所述锥套组件锁紧在所述导柱111上,所述锥套组件包括锥形外套120和锥形内套121,所述导柱111上开设有第一环形凹槽122,所述锥形内套121的内缘端嵌入所述第一环形凹槽内122,所述锥形外套120套设在所述导柱111上,所述锥形外套120的内圈开设有锥形环槽123,所述锥形内套121的外缘端嵌入所述锥形环槽123内,所述锥形外套120的底部和锁紧块119之间通过螺栓固定连接,传统的砖机生产时,模框与锁紧块是用螺栓固定的,所以两边的锁紧块的水平高度必须一样高;这样就要求锁紧块与上升导柱必须锁紧固定,不能有一点点的松动或者溜滑;将锥套内套121嵌设在第一环形凹槽122内,第一环形凹槽122的高度与锥套内套121的高度配紧配合,使锥套内套121能紧紧的镶嵌在导柱111的凹槽里,然后再把锥套外套120与锥套内套121配合并与锁紧块119用螺栓锁紧;这样不仅保证锥套外套120与锁紧块119的固定,锥套内套121与导柱111 也因为凹槽固定不会出现松动、溜滑现象;生产出来的砖才不会出现前后左右高低不平。In this embodiment, both sides of the
在本实施例中,所述振动装置102包括振动基座124,所述振动基座124安装在压模机架105的底部,所述振动基座124内设置有振动电机125,所述振动基座124的顶部安装有多个传动振动头126。In this embodiment, the
在本实施例中,所述减震装置103包括减震框127,所述减震框127安装在压模机架105上,所述减震框127和压模机架105之间形成有用于容纳锁紧块119的减震槽128,所述减震槽128的底部安装有减震弹簧129,减震装置103可以有效缓解导柱111下降时的冲击力,大大增加了设备的使用时间。In this embodiment, the
在本实施例中,所述砌砖成品输送机包括沿砌砖输送方向顺序设置的进砖输送线1、升板设备2、过渡输送线3和码垛主设备4,所述码垛主设备4的一侧设置收板设备43,所述码垛主设备4的输入端架设在过渡输送线3的输出端与收板设备43的输入端之间,所述过渡输送线3的输出端与收板设备2的输入端连接。In this embodiment, the finished brick-laying conveyor includes a brick-feeding conveying line 1, a plate-lifting
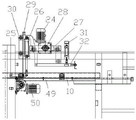
在本实施例中,所述码垛主设备4包括码垛机架6、第一推头组件7、固定板8、第二推头组件9、抽板10和托盘11,所述第一推头组件7安装在码垛机架6的输入端一侧,所述固定板8安装在码垛机架6的中部,所述抽板10可横移地安装在码垛机架6上,所述码垛机架6上设置一横移架和横移导轨49,所述横移架上安装有一横移电机50,所述横移架的顶部与抽板10连接,所述横移电机50驱动一横移转轴在横移导轨49上移动,所述横移转轴转动安装在横移架上从而带动抽板10在码垛机架6上横移,所述抽板10的输入端位于固定板8输出端的一侧,所述第二推头组件9安装在码垛机架6的中部并位于抽板10的上方,所述托盘11通过升降机构12可升降地设置在码垛机架6的输出端一侧,所述码垛机架6位于托盘11上方分别设置有用于夹住砖层的前推头13、左推头14和右推头15,所述前推头13位于第二推头组件9的前方,所述前推头13、左推头14和右推头15均由气缸控制。In this embodiment, the main stacking equipment 4 includes a stacking frame 6 , a first pusher assembly 7 , a fixing plate 8 , a
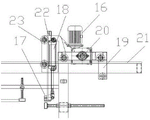
在本实施例中,所述第一推头组件7包括第一推头电机16、第一推板17、第一推板气缸18和第一推车架19,所述第一推车架19可横移地安装在码垛机架6上,所述第一推车架19上转动安装有第一推车转轴20,所述第一推头电机16安装在第一推车架19上用以驱动第一推车转轴20转动,所述第一推车转轴20的两端安装有第一滚轮,所述码垛机架6的顶部安装有供第一滚轮转动的推车轨道21,所述第一推板气缸18安装在第一推车架19上,所述第一推板气缸18的活塞端朝下设置,所述第一推板17安装在第一推板气缸18的活塞端,所述第一推板17位于第一推车架19的前方,第一推头电机16带动第一推车转轴20在推车轨道21上转动,从而带动第一推车架19在码垛机架6上移动,然后带动第一推板移动,从而推动砖层移动,第一推板气缸18可以带动第一推板17上下升降,可以根据砖层的高度调整第一推板17的高度。In this embodiment, the first push head assembly 7 includes a first push head motor 16 , a first push plate 17 , a first push plate cylinder 18 and a first cart frame 19 , the first push frame 19 It is installed on the palletizing frame 6 in a traversing manner, the first cart rotating shaft 20 is rotatably mounted on the first cart frame 19, and the first push head motor 16 is installed on the first cart frame 19 for use In order to drive the rotation of the first cart rotating shaft 20, the two ends of the first cart rotating shaft 20 are installed with first rollers, and the top of the stacking frame 6 is installed with a cart track 21 for the first roller to rotate, so The first push plate cylinder 18 is installed on the first cart frame 19 , the piston end of the first push plate cylinder 18 is arranged downward, and the first push plate 17 is installed on the piston end of the first push plate cylinder 18 , the first push plate 17 is located in front of the first cart frame 19, and the first push head motor 16 drives the first cart shaft 20 to rotate on the cart track 21, thereby driving the first cart frame 19 to stack The frame 6 moves up, and then drives the first push plate to move, thereby pushing the brick layer to move. The first
在本实施例中,所述第一推板17上安装有第一导架22,所述第一推车架19上竖直设置有与多个第一导架22相配合的第一导轮23,方便第一推板17的升降。In this embodiment, a
在本实施例中,所述第二推头组件9包括第二推头电机24、第二推板25、第二推板气缸26和第二推车架27,所述第二推车架27可横移地安装在码垛机架6上,所述第二推车架27上转动安装有第二推车转轴28,所述第二推头电机24安装在第二推车架27上用以驱动第二推车转轴28转动,所述第二推车转轴28的两端安装有第二滚轮,所述第二滚轮在推车轨道21上转动,所述第二推板气缸26安装在第二推车架27的后端,所述第二推板气缸26的活塞端朝下设置,所述第二推板25安装在第二推板气缸26的活塞端,所述第二推板25位于第二推车架27的前方,所述第二推头组件9和第一推头组件7的工作原理相同,在此不再详述。In this embodiment, the second
在本实施例中,所述第二推板25上安装有第二导架29,所述第二推车架27上竖直设置有与多个第二导架29相配合的第二导轮30,所述第二推头组件9的后端安装有第三气缸31,所述第三气缸31的活塞端朝下,所述第三气缸31的活塞端设置有隔板架32。In this embodiment, a
在本实施例中,所述升降机构12包括升降电机33、升降架34、升降链条和升降转轴36,所述升降转轴36转动安装在码垛机架6的顶部,所述升降电机33通过一电机架安装在码垛机架6的上方,所述升降电机33和升降转轴36之间通过传动链条传动连接,所述升降转轴36上设置有供升降链条套设用的升降齿轮,所述升降架34的中间设置有旋转盘37,所述升降架34的底部设置有控制旋转盘37转动的旋转减速电机38,所述托盘11放置在旋转盘37上,所述过渡输送线3将一砖板层输送至码垛主设备4的输出端,然后由第一推头组件7砖层推送至固定板8上,这是砖层和托板分离,第一推头组件7继续将砖层推送至抽板10上即复位,托板则由收板设备43输送出去,抽板10启动移动至托盘11上方,随后升降机构12带动托盘11上升使托盘11靠近抽板10,接着第二推头组件2、前推头13、左推头14和右推头15同时启动夹住砖层并定位到砖要落下的位置,随后抽板10往回走,使得砖掉落到托盘上就可以得到第一层砖层,接着降低托盘11的高度,使得托盘11上的砖高度低于抽板10的高度,第一推头组件7继续将后续的砖层推送到抽板10上,抽板10再把砖移送到托盘11的上方,抽板10往回走一定距离,头部的砖掉落在托盘11上的砖层上,然后第二推头组件2、前推头13、左推头14和右推头15松开砖层,抽板10带着砖往回移动一定距离,随后第二推头组件2、前推头13、左推头14和右推头夹住砖层,抽板10往回抽走,再使得抽板10上的砖落到第一层砖层上,这时,第二层砖层上则预留出了第一个叉车叉砖孔,然后第二推头组件2、前推头13、左推头14和右推头15松开砖层,抽板10带着尾部砖往回移动一定距离,随后第二推头组件2、前推头13、左推头14和右推头夹住砖层,抽板10往回抽走,使得尾部的砖层掉落在第一层砖层上,即可得到第二个叉车叉砖孔,后续砖层再重复第一层砖层码垛的步骤即可正常重复码垛多层砖;每当码好一层砖时,旋转减速电机38就控制旋转盘37转动90度,旋转盘37即可带动托盘11转动90度,使得相邻的两层砖摆向交错分布,提高整垛砖的稳定性。In this embodiment, the
在本实施例中,所述码垛主设备4的输出端设置有出砖设备5,所述出砖设备5包括出砖机架39、出砖电机40和出砖双轨道输送线41,所述出砖机架39安装在码垛机架6的底部,所述出砖双轨道输送线41的双轨道安装出砖机架39上并对称分布在旋转盘37的两侧,所述出砖电机40安装在出砖机架39上用以驱动出砖双轨道输送线41输送托盘11,托盘11的两侧宽度大于旋转盘37的宽度,当托盘11通过升降架34到达码垛机架6的底部时,刚好其两侧边可以搭靠在出砖双轨道输送线41上,然后由出砖电机40驱动出砖双轨道输送线41运转,托盘11则由出砖出砖双轨道输送线41输送出去,最后由工人将整剁砖进行打包后由叉车叉走。In this embodiment, the output end of the main stacking device 4 is provided with a brick ejecting device 5, and the brick ejecting device 5 includes a
在本实施例中,所述升板设备2包括升板架42、夹板机构、链条横移机构和链条升降机构,所述升板架42架设在进砖输送线1和过渡输送线3之间,所述链条横移机构安装在升板架42的顶部,所述链条升降机构安装在链条横移机构上,所述夹板机构安装在链条升降机构上,所述夹板机构由气缸控制,当砖板层到达进砖输送线1的输出端时,夹板机构通过链条横移机构和链条升降机构移动至砖板层处将其夹起并运送至过渡输送线3的输入端,所述进砖输送线1和过渡输送线3均为常规的链条输送线,在此不再详述。In this embodiment, the
在本实施例中,所述收板设备43包括入板输送线44、升降板机构45和出板输送线46,所述升降板机构45设置在入板输送线44输出端和出板输送线46输入端之间,所述出板输送线46的输入端位于升降板机构45的底部,所述升降板机构45内设置有可横移升降的抓板码垛机械勾,托板到达入板输送线44时,抓板码垛机械勾将托板逐一码垛至升降板机构上,然后由出板输送线46输送出去,所述入板输送线44和出板输送线46为常规的链条输送线,在此不再详述。In this embodiment, the
一种全自动砌块成型生产线的生产工艺,采用上述全自动砌块成型生产线,并包括以下步骤:A production process of an automatic block forming production line adopts the above-mentioned automatic block forming production line, and includes the following steps:
S1、料车装置将物料均匀的漏到下模框109中,压模油缸106控制上压架107下降;S1. The feeding truck device evenly leaks the material into the
S2、上压架107带动上压头112向下压,振动装置102同时开始振动,把下模框109内的物料压实成型;S2, the upper
S3、随后脱模油缸115启动,脱模油缸115带动同步架113上升;S3. Then the
S4、同步架113带动导柱111上升,导柱111带动锁紧块119和下模框109一起上升,下模框109上升使其与物料分离,实现脱模;S4. The synchronizing
S5、制成的砖分层放置到专用托板上进行养护处理;S5. The made bricks are placed in layers on a special pallet for maintenance treatment;
S6、将养护好的砖连托板多层一起通过叉车放置到进砖输送线1上;S6. Place the cured bricks together with the multi-layer pallets on the brick feeding conveyor line 1 through a forklift;
S7、由进砖输送线1将一层砖与板输送至升板设备2上;S7. The first layer of bricks and plates are transported to the
S8、由升板设备2将砖和板转移至过渡输送线3上;S8. The bricks and plates are transferred to the
S9、然后由过渡输送线3将砖与板输送至码垛主设备4上;S9, the bricks and plates are then conveyed to the main stacking equipment 4 by the
S10、板层通过收板设备43将其码垛收集起来;S10, the board layers are stacked and collected by the
S11、而码垛主设备4将进来的砖层码垛完成;S11, and the main stacking equipment 4 completes the stacking of the incoming brick layer;
S12、最后通过出砖设备5将其输送出去。S12. Finally, it is transported out through the brick producing device 5.
以上所述,仅为本发明的较佳实施例,并非对本发明做任何形式上的限制,任何熟悉本领域的技术人员但凡未脱离本发明技术方案的内容,依据本发明的技术实质对以上实施例所做任何简单的修改、均等变化与修饰,皆应属本发明的涵盖范围。The above are only preferred embodiments of the present invention, and are not intended to limit the present invention in any form. Any person skilled in the art, as long as they do not depart from the content of the technical solution of the present invention, can implement the above implementation according to the technical essence of the present invention. Any simple modifications, equivalent changes and modifications made in the examples should fall within the scope of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210739861.6A CN115194929A (en) | 2022-06-28 | 2022-06-28 | Full-automatic building block forming production line and production process thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210739861.6A CN115194929A (en) | 2022-06-28 | 2022-06-28 | Full-automatic building block forming production line and production process thereof |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN115194929A true CN115194929A (en) | 2022-10-18 |
Family
ID=83578605
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210739861.6A Pending CN115194929A (en) | 2022-06-28 | 2022-06-28 | Full-automatic building block forming production line and production process thereof |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115194929A (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115922877A (en) * | 2023-03-14 | 2023-04-07 | 唐山市路南登峰耐火材料有限公司 | Automatic demolding type molding equipment for producing furnace face bricks of graphite containers |
| CN118024382A (en) * | 2024-04-11 | 2024-05-14 | 泉州市益鑫机械科技有限公司 | Brick molding equipment and brick molding method |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN203449459U (en) * | 2013-08-28 | 2014-02-26 | 泉州市雄辉机械工贸有限公司 | Block machine |
| CN103737713A (en) * | 2013-12-07 | 2014-04-23 | 宁波诺亚智能设备有限公司 | Automated building block production line |
| CN103770210A (en) * | 2013-12-07 | 2014-05-07 | 宁波诺亚智能设备有限公司 | Semi-automatic brickwork maintaining line |
| CN207209429U (en) * | 2017-09-20 | 2018-04-10 | 福建泉工股份有限公司 | One kind pushes away brick stacking production line |
| CN212374374U (en) * | 2020-04-23 | 2021-01-19 | 福建群峰机械有限公司 | Low-position hole stacking production line |
| CN213732474U (en) * | 2020-08-20 | 2021-07-20 | 福建泉工股份有限公司 | Insulating brick slip casting and insulating brick pile up neatly online |
| CN113561311A (en) * | 2021-08-04 | 2021-10-29 | 泉州市益鑫机械科技有限公司 | Full-automatic building block forming production line and production method thereof |
| CN218699987U (en) * | 2022-06-28 | 2023-03-24 | 泉州市益鑫机械科技有限公司 | Full-automatic building block forming production line |
-
2022
- 2022-06-28 CN CN202210739861.6A patent/CN115194929A/en active Pending
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN203449459U (en) * | 2013-08-28 | 2014-02-26 | 泉州市雄辉机械工贸有限公司 | Block machine |
| CN103737713A (en) * | 2013-12-07 | 2014-04-23 | 宁波诺亚智能设备有限公司 | Automated building block production line |
| CN103770210A (en) * | 2013-12-07 | 2014-05-07 | 宁波诺亚智能设备有限公司 | Semi-automatic brickwork maintaining line |
| CN207209429U (en) * | 2017-09-20 | 2018-04-10 | 福建泉工股份有限公司 | One kind pushes away brick stacking production line |
| CN212374374U (en) * | 2020-04-23 | 2021-01-19 | 福建群峰机械有限公司 | Low-position hole stacking production line |
| CN213732474U (en) * | 2020-08-20 | 2021-07-20 | 福建泉工股份有限公司 | Insulating brick slip casting and insulating brick pile up neatly online |
| CN113561311A (en) * | 2021-08-04 | 2021-10-29 | 泉州市益鑫机械科技有限公司 | Full-automatic building block forming production line and production method thereof |
| CN218699987U (en) * | 2022-06-28 | 2023-03-24 | 泉州市益鑫机械科技有限公司 | Full-automatic building block forming production line |
Non-Patent Citations (3)
| Title |
|---|
| 姜玉敬等: "现代铝用炭素材料制造技术与产业研究", 31 March 2020, 冶金工业出版社, pages: 170 * |
| 张明文等: "工业机器人操作调整工", 31 August 2020, 机械工业出版社, pages: 140 - 141 * |
| 蒋清亮等: "金属热加工技术", 30 September 2012, 北京邮电大学出版社, pages: 26 * |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115922877A (en) * | 2023-03-14 | 2023-04-07 | 唐山市路南登峰耐火材料有限公司 | Automatic demolding type molding equipment for producing furnace face bricks of graphite containers |
| CN118024382A (en) * | 2024-04-11 | 2024-05-14 | 泉州市益鑫机械科技有限公司 | Brick molding equipment and brick molding method |
| CN118024382B (en) * | 2024-04-11 | 2024-07-12 | 泉州市益鑫机械科技有限公司 | Brick forming device and brick forming method |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| WO2012041058A1 (en) | Compression molding apparatus for bricks and method using the same | |
| WO2022257262A1 (en) | Brick making device and brick making process | |
| CN104070600A (en) | Production technology and production equipment of composite thermal insulation lightweight wallboard | |
| CN106827216B (en) | Brick making and brick discharging system for baking-free bricks | |
| CN109986692A (en) | A brick making machine | |
| CN107932714A (en) | A kind of full-automation brick production line | |
| CN114633347A (en) | Hydraulic product forming machine with turnover mold and manufacturing process of special-shaped concrete product | |
| CN208084649U (en) | A kind of full-automation brick production line | |
| CN218699987U (en) | Full-automatic building block forming production line | |
| CN204197920U (en) | A kind of ceramic tile board transport mechanism | |
| CN208247267U (en) | A kind of decanter type solidification case | |
| CN201304675Y (en) | Multilayer mould-pressing production device for massive flakeboard | |
| CN113561311A (en) | Full-automatic building block forming production line and production method thereof | |
| CN210501065U (en) | A thermosetting board production line | |
| CN204640493U (en) | A kind of hollow brick auto-dividing former | |
| CN209425695U (en) | One kind exempting from supporting plate static pressure block machine | |
| CN115108296A (en) | Finished brick laying conveyor and production method thereof | |
| CN216609462U (en) | Multi-port transfer distribution machine and transfer distribution equipment | |
| CN113146826B (en) | Demolding device and demoulding method for precast concrete components | |
| CN214981947U (en) | Demoulding device for concrete prefabricated part | |
| CN210436366U (en) | Non-fired brick production system | |
| CN109109132B (en) | Double-shifting-die double-station forming machine | |
| CN113580327A (en) | Building block forming host and production method thereof | |
| CN216099591U (en) | Full-automatic building block forming production line | |
| CN210061551U (en) | Brick making machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20221018 |
|
| RJ01 | Rejection of invention patent application after publication |