WO2023286737A1 - 光ファイバの製造方法および光ファイバ - Google Patents
光ファイバの製造方法および光ファイバ Download PDFInfo
- Publication number
- WO2023286737A1 WO2023286737A1 PCT/JP2022/027267 JP2022027267W WO2023286737A1 WO 2023286737 A1 WO2023286737 A1 WO 2023286737A1 JP 2022027267 W JP2022027267 W JP 2022027267W WO 2023286737 A1 WO2023286737 A1 WO 2023286737A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- optical fiber
- core
- waveguide region
- clad
- manufacturing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03C—CHEMICAL COMPOSITION OF GLASSES, GLAZES OR VITREOUS ENAMELS; SURFACE TREATMENT OF GLASS; SURFACE TREATMENT OF FIBRES OR FILAMENTS MADE FROM GLASS, MINERALS OR SLAGS; JOINING GLASS TO GLASS OR OTHER MATERIALS
- C03C13/00—Fibre or filament compositions
- C03C13/04—Fibre optics, e.g. core and clad fibre compositions
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B37/00—Manufacture or treatment of flakes, fibres, or filaments from softened glass, minerals, or slags
- C03B37/01—Manufacture of glass fibres or filaments
- C03B37/012—Manufacture of preforms for drawing fibres or filaments
- C03B37/01205—Manufacture of preforms for drawing fibres or filaments starting from tubes, rods, fibres or filaments
- C03B37/01225—Means for changing or stabilising the shape, e.g. diameter, of tubes or rods in general, e.g. collapsing
- C03B37/0124—Means for reducing the diameter of rods or tubes by drawing, e.g. for preform draw-down
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B37/00—Manufacture or treatment of flakes, fibres, or filaments from softened glass, minerals, or slags
- C03B37/01—Manufacture of glass fibres or filaments
- C03B37/02—Manufacture of glass fibres or filaments by drawing or extruding, e.g. direct drawing of molten glass from nozzles; Cooling fins therefor
- C03B37/025—Manufacture of glass fibres or filaments by drawing or extruding, e.g. direct drawing of molten glass from nozzles; Cooling fins therefor from reheated softened tubes, rods, fibres or filaments, e.g. drawing fibres from preforms
- C03B37/0253—Controlling or regulating
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B37/00—Manufacture or treatment of flakes, fibres, or filaments from softened glass, minerals, or slags
- C03B37/01—Manufacture of glass fibres or filaments
- C03B37/02—Manufacture of glass fibres or filaments by drawing or extruding, e.g. direct drawing of molten glass from nozzles; Cooling fins therefor
- C03B37/025—Manufacture of glass fibres or filaments by drawing or extruding, e.g. direct drawing of molten glass from nozzles; Cooling fins therefor from reheated softened tubes, rods, fibres or filaments, e.g. drawing fibres from preforms
- C03B37/027—Fibres composed of different sorts of glass, e.g. glass optical fibres
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/02—Optical fibres with cladding with or without a coating
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B2201/00—Type of glass produced
- C03B2201/06—Doped silica-based glasses
- C03B2201/30—Doped silica-based glasses doped with metals, e.g. Ga, Sn, Sb, Pb or Bi
- C03B2201/31—Doped silica-based glasses doped with metals, e.g. Ga, Sn, Sb, Pb or Bi doped with germanium
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B2201/00—Type of glass produced
- C03B2201/06—Doped silica-based glasses
- C03B2201/30—Doped silica-based glasses doped with metals, e.g. Ga, Sn, Sb, Pb or Bi
- C03B2201/50—Doped silica-based glasses doped with metals, e.g. Ga, Sn, Sb, Pb or Bi doped with alkali metals
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B2203/00—Fibre product details, e.g. structure, shape
- C03B2203/10—Internal structure or shape details
- C03B2203/22—Radial profile of refractive index, composition or softening point
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B2205/00—Fibre drawing or extruding details
- C03B2205/12—Drawing solid optical fibre directly from a hollow preform
- C03B2205/14—Drawing solid optical fibre directly from a hollow preform comprising collapse of an outer tube onto an inner central solid preform rod
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B2205/00—Fibre drawing or extruding details
- C03B2205/40—Monitoring or regulating the draw tension or draw rate
-
- C—CHEMISTRY; METALLURGY
- C03—GLASS; MINERAL OR SLAG WOOL
- C03B—MANUFACTURE, SHAPING, OR SUPPLEMENTARY PROCESSES
- C03B2205/00—Fibre drawing or extruding details
- C03B2205/56—Annealing or re-heating the drawn fibre prior to coating
Definitions
- the present disclosure relates to optical fiber manufacturing methods and optical fibers.
- This application claims priority based on Japanese application No. 2021-115656 filed on July 13, 2021, and incorporates all the descriptions described in the Japanese application.
- Patent Document 1 discloses an optical fiber manufacturing method for reducing the transmission loss of an optical fiber.
- a fluid for example, an inert gas
- Patent Literature 2 discloses an optical fiber manufacturing method that reduces the transmission loss of an optical fiber by drawing the optical fiber after pressurizing an optical fiber preform at a high temperature.
- Patent Document 3 discloses a treatment method for reducing the Rayleigh scattering coefficient by reducing the voids in the glass structure.
- the present disclosure provides a method for manufacturing an optical fiber.
- This optical fiber manufacturing method includes a step of heating and melting an optical fiber preform and drawing the same.
- an optical fiber is formed to include a core, a peripheral clad surrounding the core, and an outer clad surrounding the peripheral clad.
- a maximum compressive stress of at least 100 MPa is applied to the optical waveguide region including at least the core.
- the present disclosure provides an optical fiber.
- This optical fiber is an optical fiber formed to include a core, a peripheral cladding surrounding the core, and an outer cladding surrounding the peripheral cladding.
- the maximum compressive stress of the optical waveguide region including at least the core is 100 MPa or more.
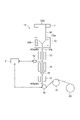
- FIG. 1 is a diagram showing the configuration of a drawing apparatus used in an optical fiber manufacturing method according to an embodiment.
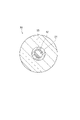
- FIG. 2 is a cross-sectional view showing an example of the cross-sectional shape of the optical fiber preform.
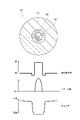
- FIG. 3 is a cross-sectional view showing an example of a cross-sectional shape of an optical fiber, and also shows refractive index distribution, power distribution, and stress distribution in the optical fiber.
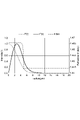
- FIG. 4 is a diagram showing a refractive index distribution, power distribution, and power distribution ⁇ radius in an optical fiber, and is a diagram for explaining an optical waveguide region.
- a method of manufacturing an optical fiber includes a step of heating and melting an optical fiber preform and drawing the same.
- an optical fiber is formed to include a core, a peripheral clad surrounding the core, and an outer clad surrounding the peripheral clad.
- a maximum compressive stress of at least 100 MPa is applied to the optical waveguide region including at least the core.
- a maximum compressive stress of at least 100 MPa or more is applied to the optical waveguide region including at least the core.
- the drawn optical fiber is strained due to the difference in thermal expansion coefficient (also called thermal expansion coefficient) in the radial direction of the material such as the glass composition and the difference in viscosity. Remain.
- thermal expansion coefficient also called thermal expansion coefficient
- void components that cause scattering in the material (for example, glass) of the optical waveguide region through which light propagates are compressed by compressive stress generated in the optical waveguide region, thereby improving the glass density of the optical waveguide region of the optical fiber.
- the manufacturing method may be carried out by a manufacturing apparatus provided with a pressurized container or the like.
- the optical waveguide region refers to a region that transmits light in an optical fiber, and includes a core and a portion of the clad surrounding it (peripheral clad).
- r ⁇ P(r) when the power distribution in the radial (r) direction of the fundamental mode of light to be transmitted is P(r), r ⁇ P(r) is 1 with respect to the peak value of r ⁇ P(r). It is the area up to the radius that is less than /100.
- r ⁇ P(r) is 1 with respect to the peak value of r ⁇ P(r).
- It may be a region up to a radius of less than /10000. Specifically, as shown in FIG. 4, when the power distribution P(r) and the refractive index distribution in the radial direction are used, the region where r ⁇ P(r) is 1/100 is approximately twice the core radius. 1/10000 is about three times the core radius.
- the first viscosity which is the viscosity at 1500° C. of the material forming the optical waveguide region
- the second viscosity which is the viscosity at 1500° C. of the material forming the outer clad.
- the tensile tension applied to the optical fiber during drawing is concentrated on the highly viscous outer clad and released after drawing.
- the compressive stress can be more reliably generated in the manufactured optical fiber by utilizing the viscosity difference between the optical waveguide region and the outer clad.
- the first viscosity may be lower than 1 ⁇ 5 of the second viscosity.
- the first thermal expansion coefficient which is the thermal expansion coefficient of the material forming the outer clad
- the thermal expansion coefficient of the material forming the optical waveguide region may be greater than the second coefficient of thermal expansion.
- the optical fiber preform is heated and melted for drawing.
- the outer cladding shrinks in the direction of reducing its volume, thereby creating compressive stress on the optical waveguide region inside the optical fiber.
- the difference in thermal expansion coefficient between the optical waveguide region and the outer cladding can be used to more reliably generate the compressive stress in the drawn optical fiber.
- the first coefficient of thermal expansion may be 1.3 times or more the second coefficient of thermal expansion.
- the first coefficient of thermal expansion of the material forming the outer cladding is greater than the second coefficient of thermal expansion of the material forming the optical waveguide region, and the material forming the optical waveguide region is may be lower than the second viscosity at 1500° C. of the material comprising the outer cladding.
- At least one of an alkali metal element, an alkaline earth metal element, a halogen element, and phosphorus is added to the material forming the optical waveguide region.
- At least one of germanium oxide, aluminum oxide, and boron oxide may be added to the material forming the outer clad.
- Two or three or all of alkali metal elements, alkaline earth metal elements, halogen elements and phosphorus may be added to the optical waveguide region. Further, by adding at least one of germanium oxide, aluminum oxide, and boron oxide to the outer clad, the coefficient of thermal expansion of the outer clad can be easily increased. Two or three of germanium oxide, aluminum oxide and boron oxide may be added to the outer cladding.
- the drawing tension for drawing the optical fiber preform may be greater than 150 gf in the drawing step.
- the compressive stress generated in the optical waveguide region can be increased, and for example, a compressive stress of 100 MPa or more can be easily generated.
- the drawing tension for drawing the optical fiber preform may be 200 gf or more.
- An optical fiber is an optical fiber formed to include a core, a peripheral clad surrounding the core, and an outer clad surrounding the peripheral clad.
- the maximum compressive stress of the optical waveguide region including at least the core is 100 MPa or more.
- the maximum compressive stress of the optical waveguide region including at least the core is 100 MPa or more.
- the drawn optical fiber remains strained due to differences in thermal expansion coefficients and viscosities in the radial direction of materials such as glass compositions.
- this strain is controlled and a large compressive stress is generated in the optical waveguide region.
- the void component that causes scattering in the material (for example, glass) of the optical waveguide region through which the light propagates is compressed by the compressive stress generated in the optical waveguide region, and the glass density of the optical waveguide region of the optical fiber can be improved. .
- this optical fiber can reduce transmission loss due to scattering.
- the optical waveguide region may be a region that is at least twice the core diameter or less. Also, the optical waveguide region may be a region that is at least three times as large as the core diameter. As a result, 99% or more of the entire single-mode transmission light power can be propagated through the low-loss glass portion, contributing to a reduction in transmission loss.
- the material forming the optical waveguide region may be doped with at least one of an alkali metal element, an alkaline earth metal element, a halogen element, and phosphorus. good.
- an alkali metal or the like By adding such an alkali metal or the like, the viscosity of glass, which is the material of the optical waveguide region, can be easily lowered, and the compressive stress in the optical fiber can be further reduced by utilizing the viscosity difference between the optical waveguide region and the outer clad. can certainly occur.
- at least one of germanium oxide, aluminum oxide, and boron oxide may be added to the material forming the outer clad.
- the coefficient of thermal expansion of the outer clad can be easily increased, and the difference in the coefficient of thermal expansion between the optical waveguide region and the outer clad can be used to more reliably generate the compressive stress in the optical fiber.
- transmission loss can be reduced more reliably.
- tensile stress may be applied to a portion of the outer clad.
- FIG. 1 is a configuration diagram of a drawing apparatus used in an optical fiber manufacturing method according to an embodiment.
- a drawing apparatus 10 shown in FIG. 1 is an apparatus for manufacturing an optical fiber 40 from an optical fiber preform 30 via glass fibers.
- the wire drawing device 10 includes a gripper 11, a heating furnace 12, a measuring device 14, a cooler 15, a die 16, an ultraviolet irradiation device 17, a direct guide roller 18, a capstan 19, a winder 20, and a control device 21.
- a heat retaining furnace 13 may be provided between the heating furnace 12 and the measuring device 14 .
- the gripping part 11 is a member for gripping the optical fiber preform 30 and feeding it into the heating furnace 12 at a constant speed.
- the optical fiber preform 30 has a base end portion 30 a that is gripped by the grip portion 11 and a tip portion 30 b that is inserted into the heating furnace 12 .
- the grip part 11 functions as a supply part that supplies the optical fiber preform 30 to the heating furnace 12 .
- the heating furnace 12 has an opening 12a into which the optical fiber preform 30 is inserted, and an opening 12b that faces the opening 12a and is pulled out as the glass fiber-like optical fiber 40a.
- the heating furnace 12 heats and melts (softens) the tip portion 30b of the optical fiber preform 30 supplied into the heating furnace 12 .
- a fiberglass-like optical fiber 40a is pulled out from the tip portion 30b melted by heating.
- the glass fiber-like optical fiber 40a is pulled out of the heating furnace 12 through the opening 12b.
- the heat-retaining furnace 13 keeps the glass fiber-like optical fiber 40a warm and relaxes the structure of the glass.
- the measuring device 14 measures the outer diameter of the optical fiber 40a in which the structure of the glass is relaxed (outer diameter of the glass).
- the measuring device 14 measures the glass outer diameter by irradiating the optical fiber 40a with a laser, for example.
- the time interval for sampling the outer diameter of the glass by the measuring device 14 is, for example, 100 ms or less. Although it depends on the drawing speed, if the sampling interval is long, there is a possibility that short-period fluctuations in the outer diameter of the glass cannot be detected.
- the measuring device 14 transmits the measured glass outer diameter to the control device 21 .
- the cooler 15 is arranged after the measuring device 14 and cools the glass-fiber-like optical fiber 40a.
- the die 16 applies resin to the outer peripheral surface of the input optical fiber 40a to form a coating resin.
- the resin includes an acrylate-based UV-curable resin.
- the UV irradiator 17 irradiates the coating resin formed on the optical fiber 40a with UV rays to cure the coating resin.
- the optical fiber 40b is formed by coating the glass fiber with the resin.
- the optical fiber 40b is sent to the capstan 19 by the guide roller 18 directly below.
- the capstan 19 pulls the optical fiber 40b at a predetermined speed and tension.
- the winder 20 winds the optical fiber 40b pulled by the capstan 19.
- the control device 21 receives the glass outer diameter measured by the measuring device 14 from the measuring device 14, and controls the winder 20 and the like based on the glass outer diameter.
- the control device 21 may control the entire drawing device 10 .
- the control device 21 includes, for example, a processor such as a CPU (Central Processing Unit), memories such as RAM (Random Access Memory) and ROM (Read Only Memory), input/output devices such as a touch panel, a mouse, a keyboard, and a display, It may be configured as a computer system including a communication device such as a network card.
- the control device 21 implements the functions of the control device 21 by operating each piece of hardware under the control of the processor based on the computer program stored in the memory.
- FIG. 2 is a cross-sectional view showing the cross-sectional structure of the optical fiber preform.
- FIG. 3 is a cross-sectional view showing a cross-sectional configuration of an optical fiber formed from an optical fiber preform, and also shows refractive index distribution, power distribution, and stress distribution in the optical fiber.
- optical fiber preform 30 comprises core 31 , peripheral clad 32 and outer clad 33 .
- the optical fiber 40 comprises a core 41 , a peripheral cladding 42 and an outer cladding 43 .
- the core 31 of the optical fiber preform 30 becomes the core 41 of the optical fiber 40
- the peripheral clad 32 of the optical fiber preform 30 becomes the core of the optical fiber 40
- the peripheral clad 42 becomes the outer clad 33 of the optical fiber preform 30 and the outer clad 43 of the optical fiber 40 .
- the core 41 and the peripheral clad 42 of the optical fiber 40 are optical waveguide regions, which are regions for transmitting light in the optical fiber 40 . In such an optical fiber 40, as shown in FIG.
- the refractive index of the core 41 is higher than that of the peripheral clad 32 and the outer clad 33, and the power of light propagating through the core 41 is It becomes stronger than the power of light propagating through the peripheral cladding 32 and the outer cladding 33 .
- the refractive index of the core 41 is higher than that of the peripheral clad 32 and the outer clad 33, and the power of light propagating through the core 41 is It becomes stronger than the power of light propagating through the peripheral cladding 32 and the outer cladding 33 .
- this embodiment by providing a difference in thermal expansion coefficient and a difference in viscosity in the material configuration in the radial direction of the optical fiber preform 30, as shown in FIG. and the peripheral cladding 42 are subjected to compressive stress. Also, a tensile stress is generated in a part of the outer clad 43 . Details of these will be described later.
- the core 31 of the optical fiber preform 30 is made of silica-based glass (SiO 2 ), for example. At least one of an alkali metal element, an alkaline earth metal element, a halogen element, and phosphorus may be added to the core 31 made of such a glass material. For example, by adding an alkali metal element, an alkaline earth metal element, a halogen element, or phosphorus to the core 31, the viscosity of the glass forming the core 31 can be lowered. Examples of alkali metal elements added to the core 31 include potassium (K), sodium (Na), lithium (Li), libidium (Rb), and cesium (Cs).
- alkaline earth metal elements added to the core 31 include magnesium (Mg), calcium (Ca), strontium (Sr), and barium (Ba).
- Phosphorus (P) can be exemplified as another element added to the core 31 .
- the metal element added to the core 31 is preferably a metal oxide, and the alkali metal oxide added to the core 31 includes K 2 O, Na 2 O, Li 2 O, Rb 2 O, Cs 2 O, Alkaline earth metal oxides may be selected from the group consisting of MgO, CaO, SrO, BaO , phosphorous oxides P2O5 , and mixtures thereof.
- the concentrations of alkali metals, alkaline earth metals, and phosphorus elements added to the core 31 may be 50 atomic ppm or more and 10000 atomic ppm or less, more preferably 100 atomic ppm, with respect to silica-based glass. It is more than 1000 atomic ppm or less.
- Fluorine (F) or chlorine (Cl) can be exemplified as the halogen element added to the core 31 .
- the concentration of the halogen element added to the core 31 may be 0.01 atomic % or more and 5 atomic % or less, more preferably 0.025 atomic % or more and 1 atomic % or less, with respect to silica-based glass.
- the core 31 can be formed by adding K 2 O, F, and Cl to silica-based glass.
- the peripheral clad 32 is a portion that covers the core 31 and constitutes an optical waveguide region together with the core 31, and is made of silica-based glass (SiO 2 ), for example. At least one of an alkali metal element, an alkaline earth metal element, a halogen element, and phosphorus may be added to the peripheral clad 32 as in the core 31 .
- the material to be added can be the same as the material of the core 31 described above, and is selected as appropriate.
- the peripheral clad 32 can be formed, for example, by adding K 2 O and F to silica-based glass.
- the outer clad 33 is a portion that surrounds the peripheral clad 32 and covers the core 31 and the peripheral clad 32, and is made of silica-based glass (SiO 2 ), for example.
- Outer cladding 33 is configured such that the refractive index of outer cladding 43 is lower than the refractive index of core 41 (see FIG. 3).
- a halogen element such as fluorine, for example, is added to the outer clad 33 .
- the outer clad 33 is made of germanium oxide (GeO 2 ), aluminum oxide (Al 2 O 3 ), boron oxide (B 2 O 3 ), etc., in order to make the coefficient of thermal expansion larger than that of the core 31 and the peripheral clad 32, for example. is added.
- the concentration of GeO 2 or the like added to the outer clad 33 may be 1 atomic % or more and 20 atomic % or less, more preferably 1 atomic % or more and 10 atomic % or less, with respect to silica-based glass.
- the outer clad 33 can be formed, for example, by adding GeO 2 and F to silica-based glass.
- the core 31 and the peripheral clad 32 are doped with at least one element selected from alkali metals, alkaline earth metals, halogen elements, and phosphorus, and the viscosity of the core 31 and the peripheral clad 32 is is low relative to the viscosity of the outer clad 33 . That is, the viscosity of the core 41 and the peripheral clad 42 when the optical fiber 40 is formed (the first viscosity that is the average value of the viscosities of the regions constituting the optical waveguide region) is different from the viscosity of the outer clad 43 (the second viscosity).
- the optical fiber preform 30 is preliminarily formed so that
- the viscosity of the optical fiber 40 referred to here is the viscosity at 1500° C., for example.
- the difference and ratio between the viscosity of the core 41 and the like and the viscosity of the outer clad 43 are not particularly limited, for example, the viscosity of the optical waveguide region such as the core 41 is lower than 1/5 of the viscosity of the outer clad 43. It may be 1/10 or less.
- the outer clad 33 is doped with GeO 2 , Al 2 O 3 or the like to increase the coefficient of thermal expansion. It is configured to have a coefficient of thermal expansion greater than that of the material from which 32 is constructed. That is, the coefficient of thermal expansion (first coefficient of thermal expansion) of the material of the outer clad 43 when the optical fiber 40 is formed is the same as the coefficient of thermal expansion of the material of the core 41 and the peripheral clad (thermal expansion of the region constituting the optical waveguide region).
- the optical fiber preform 30 is formed in advance so as to be larger than the second coefficient of thermal expansion, which is the average value of the coefficients.
- the difference or ratio between the thermal expansion coefficient of the material of the outer clad 43 and the material of the core 41 or the like is not particularly limited. It may be 1.3 times or more, or even 1.5 times or more, the thermal expansion coefficient of the material of a certain core 41 or peripheral clad 42 .
- the optical fiber preform 30 having the configuration described above can be manufactured by, for example, a VAD (Vapor Phase Axial Deposition) method.
- VAD Vapor Phase Axial Deposition
- Other methods such as MCVD (Modified Chemical Vapor Deposition) or OVD (Outside Vapor Deposition) may also be used.
- the optical fiber preform 30 is gripped by the gripping portion 11 of the drawing device 10 . Then, the tip portion 30b of the optical fiber preform 30 is inserted into the heating furnace 12 (drawing furnace), and the tip portion 30b of the optical fiber preform 30 is heated. After that, when the front end portion 30b of the optical fiber preform 30 is sufficiently heated and melted, the glass fiber-like optical fiber 40a is pulled out from the front end portion 30b.
- the drawing tension of the drawing device 10 is not particularly limited, but may be, for example, a drawing tension greater than 150 gf, and the optical fiber preform 30 is drawn with a drawing tension of 200 gf or more.
- the core 41 corresponding to the core 31 is doped with, for example, K 2 O, F, and Cl in the silica-based glass.
- K 2 O, F and Cl the viscosity of the core 41 is much lower than that of the outer clad 43 .
- K 2 O and F similarly to the cores 31 and 41, K 2 O and F, for example, are added to the silica-based glass.
- the addition of K 2 O and F significantly reduces the viscosity of the peripheral clad 32 relative to the outer clad 33 .
- the viscosity of the peripheral clad 32 may be lower than that of the core 31 .
- the outer clad 43 corresponding to the outer clad 33 for example, GeO 2 and F are added to silica-based glass.
- the coefficient of thermal expansion of the outer clad 43 is made higher than that of the core 41 .
- the coefficient of thermal expansion of the core 41 and the coefficient of thermal expansion of the peripheral clad 42 are substantially the same.
- the pulled-out glass fiber-like optical fiber 40 a is kept warm in the heat retaining furnace 13 . This relaxes the structure of the glass. Note that this heat retaining step may not be provided.
- the outer diameter of the optical fiber 40a is measured by the measuring device 14 and the optical fiber 40a is cooled by the cooler 15.
- FIG. After that, a coating layer is formed on the optical fiber 40a by the die 16, and the coating layer is cured with ultraviolet light by the ultraviolet irradiator 17 to form the optical fiber 40b.
- the optical fiber 40b on which the coating layer is formed is then wound up by the winder 20 via the guide roller 18 directly below and the capstan 19 . Thereby, the optical fiber 40 is manufactured.
- the optical fiber 40 manufactured in this manner comprises a core 41, a peripheral clad 42 surrounding the core 41, and an outer clad 43 surrounding the peripheral clad 42, as shown in FIG. Since the optical fiber 40 is formed by drawing the optical fiber preform 30 to which the various materials described above are added, the maximum compressive stress of the optical waveguide region including the core 41 and the peripheral clad 42 is 100 MPa or more. It has become.
- the core 41 corresponds to the core 31, it is made of, for example, silica-based glass (SiO 2 ). , at least one of phosphorus is added.
- the peripheral clad 42 corresponds to the peripheral clad 32, it is formed of, for example, silica-based glass (SiO 2 ), and similarly to the peripheral clad 32, an alkali metal element, an alkaline earth metal element, and a halogen element are used. , at least one of phosphorus is added.
- the viscosity of the glass constituting the core 41 and the peripheral clad 42 increases. being lowered.
- the outer clad 43 is made of silica-based glass (SiO 2 ), for example, and is configured such that the refractive index of the outer clad 43 is lower than that of the core 41 , similarly to the outer clad 33 .
- a halogen element such as fluorine is added to the outer clad 43 .
- the outer clad 43 is made of germanium oxide (GeO 2 ), aluminum oxide (Al 2 O 3 ), boron oxide (B 2 O 3 ), etc., in order to make the coefficient of thermal expansion larger than that of the core 41 and the peripheral clad 42 , for example. is added.
- germanium oxide or the like increases the coefficient of thermal expansion of the outer clad 43 in the optical fiber 40 .
- the difference in viscosity between the optical waveguide region and the outer clad 43 is used, and the difference in thermal expansion coefficient between the optical waveguide region and the outer clad 43 is used to achieve the aforementioned compression in the optical fiber 40. It is designed to generate stress more reliably.
- the viscosity of the core 41 and the peripheral clad 42 is significantly reduced with respect to the viscosity of the outer clad 43, which is a non-guiding region. Due to this viscosity difference, the tensile tension applied to the optical fiber 40 when the optical fiber preform 30 is heat-melted and drawn is concentrated on the highly viscous outer clad 43. Since the tensile strain is released, the compressive strain remains in the core 41 and the peripheral clad 42 that did not retain the tensile strain.
- compressive stress can be more reliably generated in the core 41 and the peripheral clad 42 in the manufactured optical fiber 40 by utilizing the difference in viscosity between the optical waveguide region and the outer clad.
- the coefficient of thermal expansion of the outer clad 43 is greater than the coefficients of thermal expansion of the core 41 and the peripheral clad 42 . Therefore, when the optical fiber preform 30 is heated and melted and then vitrified (that is, when the optical fibers 40a and 40b are formed), the outer clad 43 shrinks in the direction of further reducing the volume. A compressive stress will be generated in the optical waveguide region (core 41 and peripheral cladding 42) located inside.
- the difference in thermal expansion coefficient between the optical waveguide region and the outer cladding 43 is used to generate further compressive stress in the core 41 and the like in the drawn optical fiber 40, and the compression
- the value of stress is 100 MPa or more.
- the optical waveguide region is doped with at least one of alkali metal elements, alkaline earth metal elements, halogen elements, and phosphorus
- the outer clad 43 is doped with at least one of germanium oxide, aluminum oxide, and boron oxide. has been added.
- compressive stress is generated in the core 41 and the like inside the optical fiber 40 by utilizing the difference in the coefficient of thermal expansion and the difference in viscosity in the radial direction of the optical fiber. ing.
- a compressive stress of 100 MPa or more can be easily generated in the core 41 and the like of the optical fiber 40 . That is, when the optical fiber preform 30 is drawn into the optical fiber 40, the drawn optical fiber 40 is strained due to differences in thermal expansion coefficients and viscosities distributed in the radial direction of the material (glass composition). is supposed to remain.
- a large compressive stress is generated in the core 41 and the peripheral clad 42, which are optical waveguide regions.
- void components that cause scattering in the material (for example, glass) of the optical waveguide region through which light propagates are compressed by the compressive stress generated in the optical waveguide region. 40 to improve the glass density. That is, it is possible to reduce the roughness and density in the glass of the optical fiber 40 and reduce the Rayleigh scattering loss. As a result, transmission loss due to scattering in the optical fiber can be reduced.
- the compressive stress described above is generated. It reduces the transmission loss of the optical fiber. Therefore, since it is not necessary to provide a pressurized container or the like on the side of the optical fiber 40 drawing device, the optical fiber 40 with low transmission loss can be manufactured without depending on the configuration of the optical fiber manufacturing device.
- the manufacturing method according to the present embodiment it is possible to reduce the transmission loss of the optical fiber 40 without depending on the configuration of the manufacturing apparatus.
- the drawing tension for drawing the optical fiber preform 30 may be greater than 150 gf.
- the compressive stress generated in the optical waveguide region can be increased, and for example, a compressive stress of 100 MPa or more can be easily generated.
- both the difference in viscosity and the difference in thermal expansion coefficient in the radial direction of the optical fiber preform 30 and the optical fiber 40 are used to apply a pressure of 100 MPa or more to the optical waveguide region such as the core 41 of the optical fiber 40 . to reduce the transmission loss, but the present invention is not limited to this.
- the difference in viscosity in the radial direction between the optical fiber preform 30 and the optical fiber 40 may be used to generate a compressive stress of 100 MPa or more in the optical waveguide region such as the core 41 of the optical fiber 40.
- the difference in radial coefficient of thermal expansion of the material 30 and the optical fiber 40 may be used to induce a compressive stress of 100 MPa or more in an optical waveguide region such as the core 41 of the optical fiber 40 .
- the drawing tension may be adjusted to the difference between them (for example, a larger drawing tension may be applied) to generate a compressive stress of 100 MPa or more in the optical waveguide region such as the core 41 of the optical fiber 40 .
- a device for drawing the optical fiber preform 30 is provided with a mechanism (pressure vessel) for pressurizing the optical fiber, and the optical fiber preform 30 having the composition in the radial direction described above is drawn to reduce the transmission loss of the optical fiber 40. may be reduced. By combining both, the transmission loss of the optical fiber 40 can be further reduced.
- an optical fiber preform 30 having a glass structure shown in Table 1 was prepared.
- the core 31 was made of silica-based glass, and K 2 O, F, and Cl were added.
- the respective additive concentrations were 100 atomic ppm, 0.2 atomic % and 0.01 atomic % with respect to SiO 2 (reference).
- the peripheral clad 32 was made of silica-based glass, and K 2 O and F were added. Each additive concentration was 80 atomic ppm and 1.5 atomic % with respect to SiO 2 (standard).
- the outer clad 33 was made of silica-based glass, and GeO 2 and F were added. The respective additive concentrations were 2.5 atomic % and 0.7 atomic % with respect to SiO 2 (standard).
- the viscosities and thermal expansion coefficients of the core 31, the peripheral clad 32, and the outer clad 33 are shown as ratios when the value of the core 31 is set to 1. Viscosity is, for example, viscosity at 1500 degrees.
- the outer clad 33 is set so that when the optical fiber preform 30 is drawn into the optical fiber 40, the outer clad 43 is separated from the outer periphery of the core 41 of the optical fiber 40 by 20 ⁇ m or more in the radial direction.
- the core 41 diameter of the drawn optical fiber 40 was 10 ⁇ m
- the peripheral cladding 42 diameter was 50 ⁇ m
- the outer cladding 43 diameter was 125 ⁇ m.
- the above-described optical fiber preform 30 was drawn using the drawing apparatus 10 with four different drawing tensions of 50 gf, 150 gf, 250 gf and 500 gf to produce the optical fiber 40 .
- the optical fibers 40 drawn at each drawing tension correspond to Experimental Examples 1 to 4, as shown in Table 2 below.
- Table 2 shows the compressive stress generated in the core 41 and the peripheral clad 42 of each optical fiber 40 produced and the transmission loss when light with a wavelength of 1.55 ⁇ m was transmitted.
- the stress was measured by a method applying the photoelastic effect (phenomenon in which the refractive index changes according to the direction of the stress remaining in the medium).
- the peripheral clad 32 was made of silica-based glass, and only F was added. The addition concentration of F was 1.5 atomic % with respect to SiO 2 (standard).
- the outer clad 33 was made of silica-based glass, and only F was added. The concentration of F added was 1.2 atomic % with respect to SiO 2 (reference).
- Viscosity is, for example, viscosity at 1500 degrees.
- the outer clad 33 is set so that when the optical fiber preform 30 is drawn into the optical fiber 40, the outer clad 43 is separated from the outer periphery of the core 41 of the optical fiber 40 by 20 ⁇ m or more in the radial direction.
- the diameter and the like of the core 41 of the drawn optical fiber 40 were the same as those of the experimental examples described above.
- optical fiber preform 30 was drawn using the drawing device 10 with four different drawing tensions of 10 gf, 50 gf, 100 gf and 250 gf to produce the optical fiber 40 .
- the optical fibers 40 drawn at each drawing tension correspond to Experimental Examples 5 to 8, as shown in Table 4 below.
- Table 4 below shows the compression stress generated in the core 41 of each optical fiber 40 produced and the transmission loss when light with a wavelength of 1.55 ⁇ m was transmitted.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Materials Engineering (AREA)
- Geochemistry & Mineralogy (AREA)
- Life Sciences & Earth Sciences (AREA)
- Organic Chemistry (AREA)
- Manufacturing & Machinery (AREA)
- General Life Sciences & Earth Sciences (AREA)
- Optics & Photonics (AREA)
- General Physics & Mathematics (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Glass Compositions (AREA)
- Optical Fibers, Optical Fiber Cores, And Optical Fiber Bundles (AREA)
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US18/578,385 US20240375991A1 (en) | 2021-07-13 | 2022-07-11 | Method for producing optical fiber, and optical fiber |
| JP2023534793A JPWO2023286737A1 (cg-RX-API-DMAC7.html) | 2021-07-13 | 2022-07-11 | |
| EP22842081.6A EP4371952A4 (en) | 2021-07-13 | 2022-07-11 | METHOD FOR PRODUCING AN OPTICAL FIBER AND OPTICAL FIBER |
| CN202280049331.7A CN117642367A (zh) | 2021-07-13 | 2022-07-11 | 光纤的制造方法以及光纤 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2021-115656 | 2021-07-13 | ||
| JP2021115656 | 2021-07-13 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2023286737A1 true WO2023286737A1 (ja) | 2023-01-19 |
Family
ID=84919383
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2022/027267 Ceased WO2023286737A1 (ja) | 2021-07-13 | 2022-07-11 | 光ファイバの製造方法および光ファイバ |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US20240375991A1 (cg-RX-API-DMAC7.html) |
| EP (1) | EP4371952A4 (cg-RX-API-DMAC7.html) |
| JP (1) | JPWO2023286737A1 (cg-RX-API-DMAC7.html) |
| CN (1) | CN117642367A (cg-RX-API-DMAC7.html) |
| WO (1) | WO2023286737A1 (cg-RX-API-DMAC7.html) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2025249134A1 (ja) * | 2024-05-31 | 2025-12-04 | 住友電気工業株式会社 | 光ファイバ製造方法および光ファイバ製造装置 |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US12623949B2 (en) * | 2021-10-29 | 2026-05-12 | Corning Incorporated | Optical fiber draw production systems, pressure devices and methods applying pressure to optical fiber |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2005343703A (ja) * | 2004-05-31 | 2005-12-15 | Fujikura Ltd | 光ファイバ素線の製造方法、光ファイバ素線 |
| JP2007297254A (ja) * | 2006-05-02 | 2007-11-15 | Hitachi Cable Ltd | 光ファイバ |
| JP2011514877A (ja) * | 2008-03-05 | 2011-05-12 | ザ・ボーイング・カンパニー | 強度を向上させたガラス繊維 |
| WO2013073354A1 (ja) * | 2011-11-14 | 2013-05-23 | 住友電気工業株式会社 | 光ファイバおよび光伝送システム |
| WO2013140688A1 (ja) * | 2012-03-21 | 2013-09-26 | 住友電気工業株式会社 | 光ファイバの製造方法 |
| WO2015022966A1 (ja) | 2013-08-15 | 2015-02-19 | 旭硝子株式会社 | 低散乱シリカガラスおよびシリカガラスの熱処理方法 |
| CN111443424A (zh) * | 2020-05-08 | 2020-07-24 | 长飞光纤光缆股份有限公司 | 一种抗辐射保偏光纤 |
| JP2020158349A (ja) | 2019-03-27 | 2020-10-01 | 古河電気工業株式会社 | 光ファイバの製造方法 |
| JP2020169113A (ja) | 2019-04-05 | 2020-10-15 | 古河電気工業株式会社 | 光ファイバの製造方法および装置 |
| JP2021115656A (ja) | 2020-01-24 | 2021-08-10 | 株式会社大気社 | 自動ティーチングシステム |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AU773229B2 (en) * | 2000-08-28 | 2004-05-20 | Sumitomo Electric Industries, Ltd. | Optical fiber and method of making the same |
| JP2010278272A (ja) * | 2009-05-29 | 2010-12-09 | Panasonic Corp | 固体撮像素子および固体撮像素子の製造方法 |
| US8488932B2 (en) * | 2010-02-26 | 2013-07-16 | Corning Incorporated | Optical fiber with increased mechanical strength |
| US9919955B2 (en) * | 2015-07-24 | 2018-03-20 | Ofs Fitel, Llc | Optical fiber with low loss and nanoscale structurally homogeneous core |
| WO2021231083A1 (en) * | 2020-05-12 | 2021-11-18 | Corning Incorporated | Reduced diameter single mode optical fibers with high mechanical reliability |
| WO2021231085A1 (en) * | 2020-05-12 | 2021-11-18 | Corning Incorporated | Reduced diameter multimode optical fibers with high mechanical reliability |
-
2022
- 2022-07-11 JP JP2023534793A patent/JPWO2023286737A1/ja active Pending
- 2022-07-11 CN CN202280049331.7A patent/CN117642367A/zh active Pending
- 2022-07-11 WO PCT/JP2022/027267 patent/WO2023286737A1/ja not_active Ceased
- 2022-07-11 EP EP22842081.6A patent/EP4371952A4/en active Pending
- 2022-07-11 US US18/578,385 patent/US20240375991A1/en active Pending
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2005343703A (ja) * | 2004-05-31 | 2005-12-15 | Fujikura Ltd | 光ファイバ素線の製造方法、光ファイバ素線 |
| JP2007297254A (ja) * | 2006-05-02 | 2007-11-15 | Hitachi Cable Ltd | 光ファイバ |
| JP2011514877A (ja) * | 2008-03-05 | 2011-05-12 | ザ・ボーイング・カンパニー | 強度を向上させたガラス繊維 |
| WO2013073354A1 (ja) * | 2011-11-14 | 2013-05-23 | 住友電気工業株式会社 | 光ファイバおよび光伝送システム |
| WO2013140688A1 (ja) * | 2012-03-21 | 2013-09-26 | 住友電気工業株式会社 | 光ファイバの製造方法 |
| WO2015022966A1 (ja) | 2013-08-15 | 2015-02-19 | 旭硝子株式会社 | 低散乱シリカガラスおよびシリカガラスの熱処理方法 |
| JP2020158349A (ja) | 2019-03-27 | 2020-10-01 | 古河電気工業株式会社 | 光ファイバの製造方法 |
| JP2020169113A (ja) | 2019-04-05 | 2020-10-15 | 古河電気工業株式会社 | 光ファイバの製造方法および装置 |
| JP2021115656A (ja) | 2020-01-24 | 2021-08-10 | 株式会社大気社 | 自動ティーチングシステム |
| CN111443424A (zh) * | 2020-05-08 | 2020-07-24 | 长飞光纤光缆股份有限公司 | 一种抗辐射保偏光纤 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP4371952A4 |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2025249134A1 (ja) * | 2024-05-31 | 2025-12-04 | 住友電気工業株式会社 | 光ファイバ製造方法および光ファイバ製造装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| US20240375991A1 (en) | 2024-11-14 |
| EP4371952A1 (en) | 2024-05-22 |
| CN117642367A (zh) | 2024-03-01 |
| EP4371952A4 (en) | 2024-10-09 |
| JPWO2023286737A1 (cg-RX-API-DMAC7.html) | 2023-01-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2790045B1 (en) | Optical fiber and optical transmission system | |
| JP3301602B2 (ja) | 1385nmにおいて低損失を有する光ファイバとその作製法 | |
| CN107179581B (zh) | 耦合型多芯光纤 | |
| JP2014118334A (ja) | 光ファイバ製造方法 | |
| GB2423517A (en) | Apparatus for drawing and annealing an optical fibre | |
| JP2017526601A (ja) | 高塩素含有量の低減衰光ファイバー | |
| US12030804B2 (en) | Optical fiber | |
| NO153050B (no) | Fremgangsmaate til i det vesentlige kontinuerlig aa fremstille et optisk boelgelederemne og en optisk boelgeleder | |
| JP7516182B2 (ja) | 光ファイバの製造方法および装置 | |
| US20240375991A1 (en) | Method for producing optical fiber, and optical fiber | |
| CA2265975C (en) | Optical material having periodically varying refractive index and method of making | |
| TW553912B (en) | Optical fiber and preform, method of manufacturing same, and optical component made therefrom | |
| JP6916235B2 (ja) | 光ファイバの製造方法 | |
| JP5949016B2 (ja) | 光ファイバ製造方法 | |
| JP2020140080A (ja) | 光ファイバ | |
| TW200402401A (en) | Optical fiber prefrom, method for manufacturing thereof, and optical fiber obtained by drawing thereof | |
| WO2013140688A1 (ja) | 光ファイバの製造方法 | |
| JP4459720B2 (ja) | 光ファイバ素線の製造方法 | |
| JP7097325B2 (ja) | 光ファイバの製造方法および装置 | |
| US20040099015A1 (en) | Method of fabricating an optical fiber | |
| Wang | Alumina as a dopant in optical fiber by OVD | |
| US12252431B2 (en) | Quartz fibre with hydrogen barrier layer and method for the production thereof | |
| JP6175467B2 (ja) | 光ファイバ母材製造方法、光ファイバ母材及び光ファイバ | |
| WO2025249134A1 (ja) | 光ファイバ製造方法および光ファイバ製造装置 | |
| Bruce | Silica glass-based fibers |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 22842081 Country of ref document: EP Kind code of ref document: A1 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 18578385 Country of ref document: US Ref document number: 202280049331.7 Country of ref document: CN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2023534793 Country of ref document: JP |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2022842081 Country of ref document: EP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2022842081 Country of ref document: EP Effective date: 20240213 |