WO2023145932A1 - コーティング組成物、その製造方法、それを用いた被膜の製造方法、それを用いた滑液性物品キット、及びそれを用いたウォッシャー液 - Google Patents
コーティング組成物、その製造方法、それを用いた被膜の製造方法、それを用いた滑液性物品キット、及びそれを用いたウォッシャー液 Download PDFInfo
- Publication number
- WO2023145932A1 WO2023145932A1 PCT/JP2023/002857 JP2023002857W WO2023145932A1 WO 2023145932 A1 WO2023145932 A1 WO 2023145932A1 JP 2023002857 W JP2023002857 W JP 2023002857W WO 2023145932 A1 WO2023145932 A1 WO 2023145932A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- coating
- liquid
- coating composition
- lubricating liquid
- particles
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images









Classifications
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D7/00—Features of coating compositions, not provided for in group C09D5/00; Processes for incorporating ingredients in coating compositions
- C09D7/40—Additives
- C09D7/60—Additives non-macromolecular
- C09D7/61—Additives non-macromolecular inorganic
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D183/00—Coating compositions based on macromolecular compounds obtained by reactions forming in the main chain of the macromolecule a linkage containing silicon, with or without sulfur, nitrogen, oxygen, or carbon only; Coating compositions based on derivatives of such polymers
- C09D183/04—Polysiloxanes
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D5/00—Coating compositions, e.g. paints, varnishes or lacquers, characterised by their physical nature or the effects produced; Filling pastes
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D7/00—Features of coating compositions, not provided for in group C09D5/00; Processes for incorporating ingredients in coating compositions
- C09D7/20—Diluents or solvents
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D7/00—Features of coating compositions, not provided for in group C09D5/00; Processes for incorporating ingredients in coating compositions
- C09D7/40—Additives
- C09D7/60—Additives non-macromolecular
- C09D7/63—Additives non-macromolecular organic
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D7/00—Features of coating compositions, not provided for in group C09D5/00; Processes for incorporating ingredients in coating compositions
- C09D7/40—Additives
- C09D7/65—Additives macromolecular
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M169/00—Lubricating compositions characterised by containing as components a mixture of at least two types of ingredient selected from base-materials, thickeners or additives, covered by the preceding groups, each of these compounds being essential
- C10M169/04—Mixtures of base-materials and additives
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G77/00—Macromolecular compounds obtained by reactions forming a linkage containing silicon with or without sulfur, nitrogen, oxygen or carbon in the main chain of the macromolecule
- C08G77/04—Polysiloxanes
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2201/00—Inorganic compounds or elements as ingredients in lubricant compositions
- C10M2201/06—Metal compounds
- C10M2201/062—Oxides; Hydroxides; Carbonates or bicarbonates
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2201/00—Inorganic compounds or elements as ingredients in lubricant compositions
- C10M2201/10—Compounds containing silicon
- C10M2201/105—Silica
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2203/00—Organic non-macromolecular hydrocarbon compounds and hydrocarbon fractions as ingredients in lubricant compositions
- C10M2203/02—Well-defined aliphatic compounds
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2205/00—Organic macromolecular hydrocarbon compounds or fractions, whether or not modified by oxidation as ingredients in lubricant compositions
- C10M2205/16—Paraffin waxes; Petrolatum, e.g. slack wax
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2207/00—Organic non-macromolecular hydrocarbon compounds containing hydrogen, carbon and oxygen as ingredients in lubricant compositions
- C10M2207/02—Hydroxy compounds
- C10M2207/021—Hydroxy compounds having hydroxy groups bound to acyclic or cycloaliphatic carbon atoms
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2207/00—Organic non-macromolecular hydrocarbon compounds containing hydrogen, carbon and oxygen as ingredients in lubricant compositions
- C10M2207/10—Carboxylix acids; Neutral salts thereof
- C10M2207/12—Carboxylix acids; Neutral salts thereof having carboxyl groups bound to acyclic or cycloaliphatic carbon atoms
- C10M2207/125—Carboxylix acids; Neutral salts thereof having carboxyl groups bound to acyclic or cycloaliphatic carbon atoms having hydrocarbon chains of eight up to twenty-nine carbon atoms, i.e. fatty acids
- C10M2207/1253—Carboxylix acids; Neutral salts thereof having carboxyl groups bound to acyclic or cycloaliphatic carbon atoms having hydrocarbon chains of eight up to twenty-nine carbon atoms, i.e. fatty acids used as base material
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2209/00—Organic macromolecular compounds containing oxygen as ingredients in lubricant compositions
- C10M2209/10—Macromolecular compoundss obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds
- C10M2209/103—Polyethers, i.e. containing di- or higher polyoxyalkylene groups
- C10M2209/104—Polyethers, i.e. containing di- or higher polyoxyalkylene groups of alkylene oxides containing two carbon atoms only
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2213/00—Organic macromolecular compounds containing halogen as ingredients in lubricant compositions
- C10M2213/06—Perfluoro polymers
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10M—LUBRICATING COMPOSITIONS; USE OF CHEMICAL SUBSTANCES EITHER ALONE OR AS LUBRICATING INGREDIENTS IN A LUBRICATING COMPOSITION
- C10M2229/00—Organic macromolecular compounds containing atoms of elements not provided for in groups C10M2205/00, C10M2209/00, C10M2213/00, C10M2217/00, C10M2221/00 or C10M2225/00 as ingredients in lubricant compositions
- C10M2229/02—Unspecified siloxanes; Silicones
- C10M2229/025—Unspecified siloxanes; Silicones used as base material
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10N—INDEXING SCHEME ASSOCIATED WITH SUBCLASS C10M RELATING TO LUBRICATING COMPOSITIONS
- C10N2020/00—Specified physical or chemical properties or characteristics, i.e. function, of component of lubricating compositions
- C10N2020/01—Physico-chemical properties
- C10N2020/055—Particles related characteristics
- C10N2020/06—Particles of special shape or size
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10N—INDEXING SCHEME ASSOCIATED WITH SUBCLASS C10M RELATING TO LUBRICATING COMPOSITIONS
- C10N2020/00—Specified physical or chemical properties or characteristics, i.e. function, of component of lubricating compositions
- C10N2020/01—Physico-chemical properties
- C10N2020/055—Particles related characteristics
- C10N2020/061—Coated particles
-
- C—CHEMISTRY; METALLURGY
- C10—PETROLEUM, GAS OR COKE INDUSTRIES; TECHNICAL GASES CONTAINING CARBON MONOXIDE; FUELS; LUBRICANTS; PEAT
- C10N—INDEXING SCHEME ASSOCIATED WITH SUBCLASS C10M RELATING TO LUBRICATING COMPOSITIONS
- C10N2050/00—Form in which the lubricant is applied to the material being lubricated
- C10N2050/023—Multi-layer lubricant coatings
- C10N2050/025—Multi-layer lubricant coatings in the form of films or sheets
Definitions
- the present invention relates to a coating composition, a method for producing the same, a method for producing a film using the same, a synovial article kit using the same, and a washer fluid using the same.
- Patent Document 1 discloses that the component (A) has an average primary particle diameter of 1 ⁇ m or less, does not dissolve in the component (B), and does not adhere to the surface.
- Surface hydrophobic ultrafine particles having a hydrophilic functional group component (B): a volatile solvent having a boiling point of 100 ° C to 360 ° C, consisting of one or more hydrocarbon solvents and silicone solvents, component (C): (B ), a water-repellent coating containing a non-volatile silicone compound that is soluble in the volatile solvent of the component.
- the liquid falling surface with such a fine surface structure has the following problems. ⁇ Because the surface structure is fine, the mechanical durability is low. • Transmittance is generally low because the surface structure scatters light. ⁇ Because the liquid becomes spherical, surface tension acts on it, so liquids with a lower surface tension than water cannot be dropped, especially low surface energy liquids such as ethanol, acetone, and fluorine solvents. can't
- lubricant-impregnated porous underlayers have been developed as surfaces on which droplets slide down with a flat surface structure at the molecular level (for example, patent See References 2 and 3).
- SLIPS are formed of a surface lubricating liquid layer and a liquid-repellent porous underlayer for stabilizing the lubricating liquid.
- SLIPS is formed from a coating liquid containing particles, a binder resin, a lubricating liquid, and a solvent, and the lubricating liquid contained in the coating liquid has a specific property, and the volume of the lubricating liquid and the content of the binder resin It has been found that by simply applying the coating liquid onto the desired article, a coating having a synovial surface can be produced without the need for a two-step process, provided that the amounts are in specific ranges. , have completed the present invention.
- a coating composition for a coating having a synovial surface to a liquid of interest comprising: particles; a binder resin that bonds the particles together; a lubricating liquid that exhibits non-affinity with the target liquid and exhibits affinity with the binder resin; and a solvent that exhibits affinity with the lubricating liquid,
- the lubricating liquid has a contact angle of 0° when dropped on a substrate made of the same material as the particles in the air, and is dropped onto the substrate made of the same material as the particles in the target liquid.
- the contact angle is 0° when The volume ratio of the lubricating liquid to the total amount of the solvent and the lubricating liquid satisfies the range of 0.09 or more and 0.95 or less, The content of the binder resin with respect to the total amount of the solvent and the lubricating liquid satisfies the range of 0.0004 g / mL or more and 0.05 g / mL or less. coating composition.
- the coordinates of the Hansen Solubility Parameters of the solvent lie within a Hansen sphere centered on the coordinates of the Hansen Solubility Parameters of the lubricating fluid;
- the coordinates of the Hansen Solubility Parameters of the liquid of interest may lie outside the Hansen sphere centered on the coordinates of the Hansen Solubility Parameters of the lubricating liquid.
- a content of the particles with respect to the total amount of the solvent and the lubricating liquid may satisfy a range of 0.001 g/mL or more and 0.1 g/mL or less.
- a content of the particles with respect to the total amount of the solvent and the lubricating liquid may satisfy a range of 0.005 g/mL or more and 0.05 g/mL or less.
- a content of the binder with respect to a total amount of the solvent and the lubricating liquid may satisfy a range of 0.0006 g/mL or more and 0.03 g/mL or less.
- a volume ratio of the lubricating liquid to the total amount of the solvent and the lubricating liquid may satisfy a range of 0.6 or more and 0.92 or less.
- the particle size of the particles may satisfy a range of 3 nm or more and 300 nm or less.
- the particles may be made of at least one material selected from the group consisting of inorganic substances, organic substances, and composite materials thereof.
- the binder resin is at least one selected from the group consisting of silicone resin, fluororesin, epoxy resin, urethane resin, olefin resin, acrylic resin, ethylene-vinyl acetate copolymer (EVA), and polyvinyl butyral resin (PVB).
- the lubricating liquid may be at least one selected from the group consisting of silicone oil, mineral oil, vegetable oil, animal oil, heavy oil, resin, wax, fluorine oil, ionic liquid, and liquid metal.
- the solvent may be volatile at normal temperature and normal pressure.
- the solvent may be at least one selected from the group consisting of water, organic solvents, low molecular weight liquids, and mixtures thereof.
- the target liquid is water;
- the particles are at least one selected from the group consisting of silica particles, alumina particles, titania particles, and zirconia particles,
- the binder resin is a room temperature curing silicone resin,
- the lubricating liquid is silicone oil and / or fatty acid,
- the solvent may be at least one selected from the group consisting of isopropanol, hexane, ethanol, acetone, toluene, hexadecane, dimethylsulfoxide, and methyl ethyl ketone.
- a method of making a coating composition for a coating having a synovial surface with respect to a liquid of interest comprising: Particles, a binder resin that allows the particles to adhere to each other, a lubricating liquid that exhibits non-affinity with the liquid but has affinity with the binder resin, and a solvent that exhibits affinity with the lubricating liquid are mixed.
- the lubricating liquid has a contact angle of 0° when dropped on a substrate made of the same material as the particles in the air, and is dropped onto the substrate made of the same material as the particles in the target liquid.
- the contact angle at the time is 0 °
- the volume ratio of the solvent to the total amount of the solvent and the lubricating liquid satisfies the range of 0.09 or more and 0.95 or less
- the method for producing a coating composition wherein the content of the binder resin with respect to the total amount of the solvent and the lubricating liquid satisfies the range of 0.0004 g/mL or more and 0.050 g/mL or less.
- the applying is selected from the group consisting of dip coating, flow coating, flow coating, curtain coating, spin coating, spray coating, airless spray coating, bar coating, roll coating, and brush coating. You may use at least one kind of technique that is done.
- the article may have a surface made of at least one material selected from the group consisting of glass, plastic, rubber, semiconductor, metal, carbon, and ceramic.
- a synovial article kit for forming a coating having a synovial surface for a fluid of interest comprising: a coating composition as described above; and technical instructions with information for forming a synovial coating on an article using the coating composition.
- the technical instructions may include applying the coating composition onto the article to form a coating having a synovial surface with respect to the liquid of interest.
- the coating composition according to the present invention is a coating composition for coatings having a synovial surface with respect to the liquid of interest, comprising particles, a binder resin that sticks the particles together, and the liquid of interest. shows no affinity and contains a lubricating liquid showing affinity with the binder resin and a solvent showing affinity with the lubricating liquid.
- the particles are fixed by a binder resin to form a porous underlayer.
- it functions as a coating (SLIPS) having a synovial surface by disposing a lubricating liquid on the surface to form a liquid film.
- the coating composition according to the present invention can provide a film having a synovial surface simply by applying (coating) the surface of an article or the like.
- a coating composition according to the invention can also provide a synovial article kit comprising the above-described coating composition according to the invention and instructions.
- a coating composition according to the present invention can also provide a washer fluid containing the coating composition of the present invention.
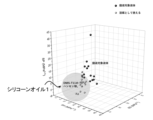
- FIG. 5 is a Hansen Solubility Parameter sphere for silicone oil 1 of Table 5;
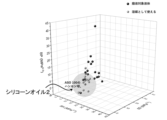
- FIG. 5 is a Hansen Solubility Parameter sphere for silicone oil 2 of Table 5;
- 5 is a Hansen Solubility Parameter sphere for oleic acid in Table 5.
- FIG. 1 is a flow chart showing a process for producing a coating having a synovial surface using a coating composition.
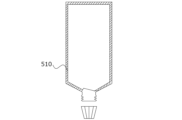
- 1 is a schematic diagram showing a food container provided with a coating having a synovial surface using a coating composition;
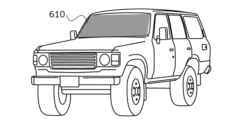
- FIG. 1 is a schematic diagram showing a motor vehicle with a coating having a synovial surface using the coating composition;
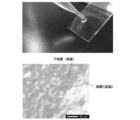
- FIG. 1 is a diagram showing the state of a coating formed from the composition of Example 1.
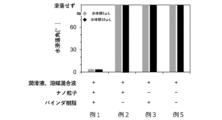
- FIG. 1 shows the water slide fall angle on coatings formed from the compositions of Examples 1-3 and 5.
- FIG. 1 is a diagram showing the contact angle between a substrate made of particles of Example 1 and a lubricating liquid.
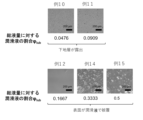
- FIG. FIG. 10 is a diagram showing coatings formed from the compositions of Examples 10 to 15.
- FIG. FIG. 2 is a graph showing the dependence of the water contact angle and water sliding angle on the coatings formed from the compositions of Examples 1 and 6 to 20 on the lubricating liquid proportion.
- FIG. 2 is a graph showing the dependence of the water contact angle and water sliding angle on coatings formed from the compositions of Examples 1 and 6 to 20, and on the proportion of lubricating liquid.
- FIG. 1 is a diagram showing the contact angle between a substrate made of particles of Example 1 and a lubricating liquid.
- FIG. 10 is a diagram showing coatings formed from the compositions of Examples 10 to 15.
- FIG. 2 is a graph showing the dependence of the water contact angle and water sliding angle on the coatings formed
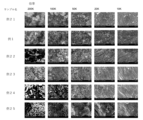
- FIG. 2 shows SEM images of the porous underlayers of coatings formed from the compositions of Examples 1 and 21-25.
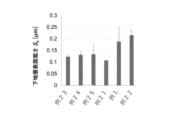
- FIG. 2 shows the surface roughness of the porous underlayers of the coatings formed from the compositions of Examples 1 and 21-25.
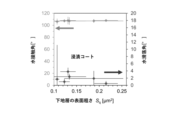
- FIG. 2 is a diagram showing the dependence of the water contact angle and water sliding angle of coatings formed from the compositions of Examples 1 and 21 to 25 on the surface roughness of the porous underlayer.
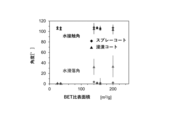
- FIG. 2 is a diagram showing the BET specific surface area dependence of particles of water contact angles and water sliding angles of films formed from the compositions of Examples 1 and 21 to 25.
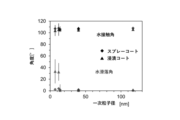
- FIG. FIG. 2 is a diagram showing particle size (primary particle size) dependence of the water sliding fall angle of films formed from the compositions of Examples 1 and 21 to 25.
- FIG. 10 shows self-healing properties of coatings formed from the coating composition of Example 1.
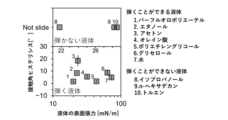
- FIG. 10 is a diagram showing the relationship between the contact angle hysteresis and the surface tension of the coating formed from the coating composition of Example 34 and various liquids.
- FIG. 10 is a diagram showing the contact angle between a substrate made of particles of Example 34 and a lubricating liquid.
- FIG. 10 shows the liquid of interest sliding down a coating formed from the coating composition of Example 34.
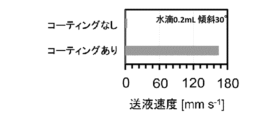
- FIG. Figure 2 shows the synovial properties of coatings using the coating composition of Example 1 formed on various articles. It is a figure which shows the change of the liquid feeding speed in a silicone tube.
- FIG. 10 is a diagram showing a state of a shower test with and without a film on a window of an automobile.
- Liquid-repellent technology which is a technology that repels liquid on the surface of a substrate, involves forming droplets on the surface and restricting the area where the droplets come in contact with the surface. ) and a phenomenon in which a droplet formed on the surface slides down the surface (sliding).
- falling is the technique shown in Patent Document 1.
- Sliding is a technique shown in Patent Documents 2 and 3, and its surface is called SLIPS. Falling and sliding are completely different mechanisms.
- SLIPS liquid repellent technology that utilizes sliding down, and by controlling the structure and composition of the composition, SLIPS, that is, a coating having a synovial surface against the target liquid (hereinafter referred to as , simply referred to as a coating or a SLIPS coating) has been developed.
- a synovial surface means that a drop of 5 ⁇ L of a droplet is dropped on the surface of a film formed on a glass plate, and the sliding angle of the droplet is 40° or less when the glass plate is tilted.
- the coating composition of the present invention includes particles, a binder resin that bonds the particles to each other, and a lubricating liquid that exhibits non-affinity with the target liquid, and a lubricating liquid that exhibits affinity with the binder resin. and the indicated solvent.
- a binder resin that bonds the particles to each other
- a lubricating liquid that exhibits non-affinity with the target liquid
- a lubricating liquid that exhibits affinity with the binder resin. and the indicated solvent.
- the particles become the porous underlayer 420 in FIG. 4, which will be described later, and the material is not particularly limited, and desired particles can be used.
- the particles may preferably consist of at least one material selected from the group consisting of inorganic substances, organic substances, and composite materials thereof. For example, if you want to obtain a film that is transparent in the visible region, it is preferable to select particles whose refractive index is close to the refractive index of the lubricant. should be selected.
- the composite material may be an organic-inorganic hybrid, a hybrid of nonmetal and metal, an organic metal material, or a combination of three or more different materials. Also, one material is encapsulated in the other material to form one particle, one material penetrates the other material to form one particle, and hemispherical different Materials that are combined to form a single particle are also composite materials. Exemplary particle materials are shown in Table 1.
- the particle size of the particles is not particularly limited because available particles can be used, but illustratively, it may be in the range of 3 nm or more and 300 nm or less. Within this range, particles of the above material are readily available.
- the particle size of the particles preferably satisfies the range of 5 nm or more and 200 nm or less. Within this range, it is easy to form the porous underlayer 420 described with reference to FIG.
- the particle size of the particles more preferably satisfies the range of 5 nm or more and 150 nm or less.
- the BET specific surface area of the particles is not particularly limited, for example, particles that satisfy the range of 20 m 2 /g or more and 250 m 2 /g or less are preferably adopted.
- the lubricating liquid is easily impregnated and the lubricating liquid is easily retained on the surface, so that the liquid film 430 can be easily formed in FIG. 4 to be described later.
- the surface of the particles may be modified with functional molecules.
- Examples of such functional molecules are those shown in Table 1, but are not limited thereto.
- the surface can be made hydrophobic by modifying the particles with functional molecules having functional groups such as alkyl groups, fluoroalkyl groups, polymethylsiloxane groups, and phenyl groups.
- the surface can be made hydrophilic by modifying the particles with functional molecules having functional groups such as amino groups, amide groups, hydroxyl groups, aldehyde groups, and thiol groups. Functional molecules that modify the surface of particles can be appropriately selected by those skilled in the art.
- the binder resin may be either a thermosetting resin or a thermoplastic resin, as long as it functions to bond the particles together. Anything is preferred. From such a point of view, a room temperature curing resin is preferable. The room temperature is in the range of 5°C or higher and 35°C or lower.
- Binder resin Exemplary binder resins are selected from the group consisting of silicone resins, fluorine resins, epoxy resins, urethane resins, olefin resins, acrylic resins, ethylene-vinyl acetate copolymers (EVA), and polyvinyl butyral resins (PVB). may be at least one type of
- the silicone resin may be, for example, a polymer having a skeleton of polyalkylhydrogensiloxane, polydialkylsiloxane, preferably polysilsesoxane or polydimethylsiloxane, and one end of linear or branched polydimethylsiloxane. Also includes modified silicone resins having substituents on both ends and side chains.
- fluororesins examples include polytetrafluoroethylene (PTFE), tetrafluoroethylene/hexafluoropropylene copolymer (FEP), tetrafluoroethylene/perfluoroalkyl vinyl ether copolymer (PFA), polyvinylidene fluoride (PVDF ), polychlorotrifluoroethylene (PCTFE), tetrafluoroethylene-ethylene copolymer (ETFE), fluoroethylene vinyl ether (FEVE), or ethylene chlorotrifluoroethylene copolymer (ECTFE).
- PTFE polytetrafluoroethylene
- FEP tetrafluoroethylene/hexafluoropropylene copolymer
- PFA tetrafluoroethylene/perfluoroalkyl vinyl ether copolymer
- PVDF polyvinylidene fluoride
- PCTFE polychlorotrifluoroethylene
- ETFE tetrafluoroethylene-
- epoxy resin those having two or more epoxy groups in one molecule are employed, and examples thereof include bisphenol A type (which may be brominated), bisphenol F type, bisphenol S type, diphenyl ether type, hydroquinone type, and naphthalene. type, biphenyl type, fluorene type, phenol novolac type, ortho-cresol novolak type, trishydroxyphenylmethane type, trifunctional type, tetraphenylolethane type, dicyclopentadiene phenol type epoxy resin.
- bisphenol A type which may be brominated
- bisphenol F type bisphenol S type
- diphenyl ether type diphenyl ether type
- hydroquinone type and naphthalene.
- naphthalene biphenyl type, fluorene type, phenol novolac type, ortho-cresol novolak type, trishydroxyphenylmethane type, trifunctional type, tetraphenylolethane type, dicycl
- the urethane resin may be a copolymer of polyol and isocyanate.
- the olefin resin may be a polymer or copolymer such as polyethylene, polypropylene, and chlorinated polyethylene.
- acrylic resins include polymers or copolymers such as methyl methacrylate, isopropyl methacrylate, ethyl methacrylate, methyl acrylate, ethyl acrylate, isopropyl acrylate, n-butyl acrylate, 2-ethylhexyl acrylate, and n-butyl methacrylate. good.
- the lubricating liquid impregnates the porous underlayer 420 in FIG. 4, which will be described later, and forms a liquid film 430 on the porous underlayer.
- the lubricating liquid is not particularly limited as long as it shows non-affinity for the target liquid and shows affinity for the above binder resin.
- the lubricating liquid and the target liquid are mixed, if two-layer separation can be visually confirmed, it is judged that the lubricating liquid exhibits non-affinity for the target liquid.
- the Hansen solubility parameter is the solubility parameter introduced by Hildebrand divided into three components, the dispersion term, the polar term, and the hydrogen bond term, and expressed in a three-dimensional space.
- the dispersion term indicates the effect of the dispersion force
- the polar term indicates the effect of the dipole force
- the hydrogen bond term indicates the effect of the hydrogen bond force.
- the contact angle of the lubricant when the contact angle of the lubricant is 30° or less when the lubricant is dropped onto the surface of the binder resin in the air, it is judged that the lubricant exhibits affinity with the binder resin. More preferably, the contact angle is 10° or less.
- the lubricating liquid is uniformly mixed with the binder resin, and when the porous underlayer 420 is formed, the porous underlayer 420 can be sufficiently impregnated with the lubricating liquid.
- the lubricating liquid is preferably at least one selected from the group consisting of silicone oil, mineral oil, vegetable oil, animal oil, heavy oil, resin, wax, fluorine oil, ionic liquid, and liquid metal. These can meet the above conditions depending on the choice of liquid and binder resin in question.
- Table 2 shows representative lubricating liquids among these lubricating liquids. The lubricating liquids shown in Table 2 are illustrative and not limiting.
- modified silicone oils may be used.
- modified silicone oils include amino-modified, epoxy-modified, carboxy-modified, carbinol-modified, methacrylic-modified, mercapto-modified, and phenol-modified silicone oils.
- the lubricating liquid it is preferable to select a substance that has a structure similar to that of the binder resin, as this will increase affinity.
- a combination of silicone resin as the binder resin and silicone oil as the lubricating liquid may be used.
- the solvent is not particularly limited as long as it functions to stably retain the particles, binder resin, and lubricating liquid described above and exhibits affinity with the lubricating liquid.
- the solvent preferably exhibits volatility at normal temperature and normal pressure. As a result, the solvent evaporates under normal circumstances, so in FIG. 4 described later, simply applying the coating composition of the present invention to the article allows the formation of a synovial film by a one-step coating process.
- "normal temperature” refers to 20°C (293K)
- normal pressure refers to 1 atm (absolute pressure).
- the solvent having volatility at normal temperature and normal pressure is a solvent having a vapor pressure of less than 10 Pa at 20° C. and 1 atm.
- a solvent exhibits affinity for a lubricating liquid if the Hansen Solubility Parameter coordinates of the solvent lie within the Hansen sphere centered on the Hansen Solubility Parameter coordinates of the lubricating liquid.
- the solvent may be, for example, at least one selected from the group consisting of water, organic solvents, low-molecular-weight liquids, and mixtures thereof. Representative solvents among these solvents are exemplified in Table 3. By appropriately selecting the lubricating liquid and solvent, the above conditions can be met.
- each lubricating liquid (0.1 mL) and each solvent/liquid (0.1 mL) are mixed, stirred well, and if two-layer separation or cloudy state is observed after 5 minutes, non-affinity (0 ), and if no two-layer separation and cloudy state were observed, it was determined to exhibit affinity (1).
- the lubricating liquid and solvent may be selected as appropriate for the target liquid.
- affinity or non-affinity can be determined using the Hansen sphere centered on the coordinates of the Hansen solubility parameter of the lubricating liquid.
- Table 5 shows the Hansen solubility parameter, the radius of the Hansen sphere, etc. of the representative lubricating fluids described above.
- Table 6 shows the Hansen Solubility Parameters for representative solvents/liquids. The definition and calculation of the Hansen Solubility Parameter is provided by Charles M. Hansen, "Hansen Solubility Parameters; A Users Handbook, Second Edition (CRC Press, 2007)".
- Hansen Solubility Parameters in Practice HSPiP
- the Hansen solubility parameters can be easily estimated from the chemical structure of various liquids for which literature values are unknown.
- literature values were used for the Hansen solubility parameters in this specification.
- the affinity/non-affinity between a liquid or solvent and a lubricating liquid can be determined from equation (1) or (2) below.
- D sol , P sol , and H sol are the dispersion, polar, and hydrogen bonding terms of the solvent or liquid, respectively
- D lub , P lub , and H lub are the dispersion of the lubricating liquid, respectively.
- term, polar term, and hydrogen bonding term, and R is the radius of the Hansen sphere of the lubricating fluid.
- the solvent and lubricant satisfy equation (1) (i.e., the Hansen Solubility Parameter coordinates of the solvent lie within the Hansen sphere centered on the Hansen Solubility Parameter coordinates of the lubricant), then the solvent and lubricant can be judged to have affinity, and the lubricating liquid and the solvent can be uniformly mixed and used as the solvent.
- the liquid and the lubricating liquid satisfy equation (2) (i.e., the coordinates of the Hansen Solubility Parameters of the liquid lie outside the Hansen sphere centered on the coordinates of the Hansen Solubility Parameters of the lubricating liquid), then the liquid and the lubricating liquid It can be determined that it has no affinity with liquids, and lubricating liquids can repel liquids.
- Figures 1 to 3 show the results of calculating the relationship between formulas (1) and (2) for representative lubricating liquids and solvents or liquids.
- FIG. 1 is a Hansen Solubility Parameter sphere for silicone oil 1 in Table 5.
- FIG. 2 is a Hansen Solubility Parameter sphere for silicone oil 2 of Table 5.
- FIG. 3 is a Hansen Solubility Parameter sphere for oleic acid from Table 5.
- the area shown in dark grayscale is the Hansen sphere of the selected lubricating fluid. Solvents located within the Hansen sphere show affinity with the lubricating liquid, and liquids located outside the Hansen sphere show no affinity with the lubricating liquid. As illustrated in FIGS. 1-3, there are a myriad of choices for lubricating fluids and liquids or solvents, but those skilled in the art will be able to demonstrate an incompatibility with the liquid of interest as required. , a lubricating liquid having an affinity for the solvent can be appropriately selected.
- the lubricating liquid contained in the coating composition of the present invention has a contact angle of 0° when dropped on a substrate made of the same material as the particles in the air.
- the contact angle is measured by dropping the selected lubricating liquid onto a substrate made of the same material as the selected particles in accordance with JIS R 3257, and is the final contact angle after sufficient time has passed.
- the substrate used for evaluation may or may not be porous.
- the lubricating liquid contained in the coating composition of the present invention has a contact angle of 0° when dropped onto a substrate made of the same material as the particles in the target liquid. As a result, in FIG. 4, which will be described later, the target liquid slides down on the surface of the liquid film 430 made of the lubricating liquid.
- the contact angle is the same as the contact angle measurement method described above except that it is in liquid, and is the final contact angle after sufficient time has elapsed.
- the volume ratio of the lubricating liquid to the total amount of the solvent and the lubricating liquid satisfies the range of 0.09 or more and 0.95 or less. If the volume ratio of the lubricating liquid to the total amount of the solvent and the lubricating liquid is less than 0.09, the amount of the lubricating liquid is too small to form the liquid film 430 and the synovial properties are not exhibited.
- the volume ratio of the lubricating liquid to the total amount of the solvent and the lubricating liquid exceeds 0.95, the amount of the lubricating liquid is large, so that the ratio of the particles and the binder resin is relatively decreased, and the lubricating liquid is spread over the porous underlayer 420.
- the film consisting of becomes unstable.
- the volume ratio of the lubricating liquid to the total amount of the solvent and lubricating liquid preferably satisfies the range of 0.16 or more and 0.95 or less. Within this range, a SLIPS coating transparent to visible light can be formed. In the present specification, "transparent to visible light” means having a transmittance of 85% or more for a wavelength of 550 nm.
- the volume ratio of the lubricating liquid to the total amount of the solvent and lubricating liquid is more preferably in the range of 0.6 or more and 0.92 or less. Within this range, the sliding angle can be 1° or less, resulting in an excellent SLIPS coating.
- the coating composition of the present invention satisfies the range of 0.0004 g/mL or more and 0.05 g/mL or less of the binder resin content with respect to the total amount of the solvent and the lubricating liquid. If the content of the binder resin with respect to the total amount of the solvent and lubricating liquid is less than 0.0004 g/mL or exceeds 0.05 g/mL, the amount of the binder resin is inappropriate and the porous underlayer 420 cannot be formed.
- the content of the binder resin with respect to the total amount of the solvent and lubricating liquid is preferably in the range of 0.0006 g/mL or more and 0.03 g/mL or less. Within this range, the formation of the porous underlayer 420 can be promoted.
- the content of the binder resin with respect to the total amount of the solvent and lubricating liquid is more preferably in the range of 0.1 g/mL or more and 0.5 g/mL or less. Within this range, the porous underlayer 420 has a high transmittance.
- the content of particles is not limited, but the content of particles with respect to the total amount of solvent and lubricating liquid preferably satisfies the range of 0.001 g/mL or more and 0.1 g/mL or less. . Thereby, the formation of the porous underlayer 420 can be promoted.
- the content of particles relative to the total amount of solvent and lubricating liquid is more preferably in the range of 0.005 g/mL or more and 0.05 g/mL or less. Within this range, a good quality porous underlayer 420 is formed.
- the content of the particles relative to the total amount of solvent and lubricating liquid is more preferably in the range of 0.005 g/mL or more and 0.02 g/mL or less. Within this range, the porous underlayer 420 has a high transmittance and the SLIPS coating has a small sliding angle.
- the coating composition of the present invention preferably contains at least one particle selected from the group consisting of silica particles, alumina particles, titania particles, and zirconia particles, and a room-temperature-curable
- a binder resin that is a silicone resin, a lubricant that is a silicone oil and/or a fatty acid, and at least one solvent selected from the group consisting of isopropanol, hexane, ethanol, acetone, toluene, hexadecane, dimethylsulfoxide, and methyl ethyl ketone, should contain Since these combinations can satisfy the above conditions, a SLIPS coating can be formed and water can slide down.
- the target liquid other than water may be any liquid such as the above-described solvent, lubricating liquid, or drug.
- a method for producing the coating composition of the present invention will be described.
- the manufacturing method of the coating composition of the present invention simply satisfies the above-mentioned conditions, the particles constituting the porous underlayer, the binder resin for binding the particles to each other, and the non-affinity for the target liquid. It suffices to mix a lubricating liquid exhibiting properties and affinity with the binder resin and a solvent exhibiting affinity with the lubricating liquid.
- the particles, the binder resin, the lubricating liquid, and the solvent are the same as described above, so their description is omitted.
- FIG. 4 is a flow chart showing the manufacturing process of a coating having a synovial surface using the coating composition of the present invention.
- a coating having a synovial surface is formed on the article, so prepare the article 410 on which the coating is to be formed.
- the coating composition of the present invention may be applied to the prepared article 410 (step S410).
- the inventors have found that simply applying the coating composition of the present invention onto the desired article 410 can form a coating 440 having a synovial surface.
- the solvent begins to volatilize.
- particles begin to deposit on the surface of the article 410 , and the particles adhere to each other by the binder resin to form the porous underlayer 420 .
- the lubricating liquid impregnates the formed porous underlayer 420 composed of particles, precipitates on the particle surface (the surface of the porous underlayer 420), and coalesces. This becomes the liquid film 430 on the porous underlayer 420 .
- coating 440 with a synovial surface can be provided by simply coating the coating composition of the present invention onto desired article 410 .
- the article 410 may be heated along with the application of the composition. This can promote volatilization of the solvent.
- the environment surrounding article 410 may be depressurized along with application of the composition. This can promote volatilization of the solvent.
- heating and pressure reduction may be used in combination.
- the article 410 is shown as a flat plate in FIG. 4 for simplicity, the article is not limited to a flat plate.
- the surface of the article 410 is not limited as long as the coating composition can be applied thereon, and may be, for example, a curved surface, a curved surface, or an uneven surface.
- the material of the article 410 is not limited as long as the coating composition of the present invention can be applied, but from the viewpoint of adhesion, at least one selected from the group consisting of glass, plastic, rubber, semiconductors, metals, carbon, and ceramics. It is preferable to have a surface made of a material of
- the glass is not limited to silicate glass (including soda lime glass, borosilicate glass, and quartz) containing silicate as a main component, but may be acrylic glass, chalcogenide glass, metallic glass, or organic glass.
- Plastic is a so-called synthetic resin.
- the rubber may be either natural rubber or synthetic rubber.
- the semiconductors may be silicon semiconductors, germanium semiconductors, compound semiconductors such as GaAs, GaP, InP, InGaAs.
- the metal may be a single metal, or may be an alloy such as stainless steel.
- Carbon may be a carbon fiber laminate, carbon fiber reinforced plastic (CFRP), or carbon fiber reinforced composite material.
- Ceramics are sintered bodies obtained by heating and sintering inorganic substances, and may be, for example, metal or non-metal oxides, carbides, nitrides, borides, oxynitrides, oxyborides, and the like.
- the method of application is not particularly limited, and known techniques can be used. At least one method selected from the group consisting of coating, roll coating, and brushing can be used.
- Drying is not essential, but it may be dried for the purpose of promoting the formation of a film or under special circumstances. Drying may be, for example, heating, air drying (including hot air and cold air), freeze drying, and the like.
- the surface of the article 410 may be cleaned prior to applying the coating composition.
- the cleaning may be cleaning with water, alcohol, or the like. This may remove surface contaminants and improve adhesion between article 410 and SLIPS coating 440 .
- the synovial article kit of the present invention comprises the coating composition of the present invention and technical instructions.
- the technical instructions for applying the coating composition to the article and forming a synovial film on the surface of the article are recorded.
- a coating having synovial properties can be formed on a desired article surface.
- Description of the coating composition is omitted because it is as described above.
- the method for forming a coating having a synovial surface using the coating composition described above applies.
- technical instructions in which the above-mentioned information is recorded are, for example, computer-readable recording media such as magnetic recording media, optical recording media, and semiconductor memories, media such as paper, film, and fabric. It's okay.
- the form of recording in the technical instructions is not particularly limited, and may be recorded so as to be directly readable by humans and/or computers, or readable through communication lines such as the Internet.
- Means for example, a URL of a document describing a method of applying the coating composition, a (two-dimensional) barcode describing the URL, etc.
- the term "record” includes information printed on a paper medium and the like.
- a typical synovial article kit includes, for example, a container, a coating composition housed in the container, and a label seal attached to the container.
- the seal may be in the form of a label seal that describes how to apply the coating composition to the article. Examples of the "method for applying the coating composition" described on the label seal include a preferable application method, the type of target liquid, and the like.
- FIG. 5 is a schematic diagram showing a food container with a coating 510 having a synovial surface using the coating composition.
- the food contained in the food container is mayonnaise dressing
- the target liquid is mayonnaise dressing.
- the coating composition for forming a film having a synovial surface on a mayonnaise dressing include, for example, silica nanoparticles as particles, polydimethylsiloxane as a binder resin, silicone oil as a lubricating liquid, isopropanol as a solvent, A coating composition containing
- the coating composition of the present invention is applied to the inner wall of a food container according to the method for producing a coating having a synovial surface of FIG. A coating 510 having a surface is formed.
- the target liquid (mayonnaise dressing in this case) slides down on the inner wall of the food container, so that the user can use it up to the end without remaining in the food container. No cleaning is required.
- FIG. 6 is a schematic diagram showing an automobile provided with a coating 610 having a synovial surface using the coating composition.
- the target liquid is water such as rain or snow.
- the coating composition of the present invention is applied to the windshield of an automobile to form a coating 610 having a synovial surface on the windshield surface.
- the target liquid here, water such as rain
- the coating 610 having a synovial surface obtained in this manner has self-healing properties, the coating does not break even when rubbed by a wiper, and has excellent durability.
- the coating composition of the present invention can be used to clean automobile windshields because the coating composition of the present invention can be simply applied onto the desired article to form a film having a synovial surface.
- a coating 610 having a synovial surface can be formed by using it as a washer fluid for the.
- Binder resin The following were used as binder resin. Both are silicone resins having a polydimethylsiloxane skeleton. ⁇ One-liquid room temperature vulcanizing (RTV) silicone rubber (DOWSIL (registered trademark) HC 2100 manufactured by Dow Chemical Company) ⁇ Two-liquid room temperature vulcanizing (RTV) silicone rubber (manufactured by Dow Chemical Company, SYLGARD (registered trademark) 184 Silicone Elastomer Kit)
- Binder Resin The following were used as solvents, liquids, or lubricating liquids. ⁇ Isopropanol (manufactured by FUJIFILM Wako Pure Chemical Industries, Ltd.) ⁇ Hexane (manufactured by FUJIFILM Wako Pure Chemical Industries, Ltd.) ⁇ Ethanol (manufactured by FUJIFILM Wako Pure Chemical Industries, Ltd.) ⁇ Dichloropentane fluoropropane (manufactured by AGC Co., Ltd., Asahiklin (registered trademark) AK-225) ⁇ Acetone (manufactured by FUJIFILM Wako Pure Chemical Industries, Ltd.) ⁇ Toluene (manufactured by FUJIFILM Wako Pure Chemical Industries, Ltd.) ⁇ n-hexadecane (manufactured by Fujifilm Wako Pure Chemical Industries, Ltd.) ⁇ Ultrapure water
- Examples 1 to 44 [Preparation of coating composition]
- various coating compositions were prepared and used to form coatings. Specifically, the nanoparticles, the binder resin, the solvent, and the lubricating liquid were each weighed so as to satisfy the compounding components and compounding compositions shown in Tables 7 to 17, and stirred with a magnetic stirrer at room temperature (20°C). , a coating composition was prepared.
- the resulting coating composition was applied to a glass plate (size 1.0 ⁇ 26 ⁇ 76 mm, manufactured by Mutoh Chemical Co., Ltd.) to prepare a coating (step S410 in FIG. 4). Application was carried out by spraying the coating composition (spray coating) or by immersing the glass plate in the coating composition (dip coating).
- Example 1 The state of the coating obtained in Example 1 was observed with a scanning electron microscope (FE-SEM, S-4800 manufactured by Hitachi High-Tech Co., Ltd.). The observation results are shown in FIG. Further, the observation results of the coatings obtained in Examples 10-12 and Examples 14-15 are shown in FIG.
- FIG. 7 is a diagram showing the appearance of a coating using the coating composition of Example 1.
- FIG. 8 is a diagram showing the water slide angle of films formed from the coating compositions of Examples 1 to 3 and Example 5.
- FIG. 7 is a diagram showing the appearance of a coating using the coating composition of Example 1.
- FIG. 8 is a diagram showing the water slide angle of films formed from the coating compositions of Examples 1 to 3 and Example 5.
- FIG. 8 is a diagram showing the appearance of a coating using the coating composition of Example 1.
- FIG. 8 is a diagram showing the water slide angle of films formed from the coating compositions of Examples 1 to 3 and Example 5.
- Example 1 when water droplets were dropped onto the glass plate to which the coating composition of Example 1 was applied by spraying, it was confirmed that the water droplets slid down, indicating that a synovial surface was formed on the glass plate. understood.
- the SEM image revealed that the synovial surface consisted of a rough porous underlayer and a liquid film formed thereon. Since the solvent is volatile at normal temperature and normal pressure, the liquid film is a lubricating liquid. This indicates that the coating composition of Example 1 is a coating composition that forms a film having a synovial surface with respect to the liquid of interest (here, water).
- silicone oil 1 which is the lubricating liquid
- silicone oil 1 shows no affinity for water, which is the target liquid, but has affinity for isopropanol, which is the solvent. I confirmed that it shows sex.
- One-liquid RTV silicone rubber which is a binder resin, is a chemical substance similar to silicone oil 1 and exhibits affinity for lubricating liquids. Isopropanol is known to volatilize at normal temperature and normal pressure.
- the coating compositions of Examples 2-3 and 5 which contained only a portion of these, did not form surfaces with synovial properties.
- the coating composition of Example 4 which does not contain lubricating fluid, is similar to that of US Pat. From this, it was shown that the coating composition for forming the SLIPS coating contains particles, binder resin, lubricating liquid, and solvent as essential components.
- FIG. 9 is a diagram showing the contact angle between the substrate made of the particles of Example 1 and the lubricating liquid.
- FIG. 9(A) shows the state after 7 seconds have elapsed after dropping silicone oil 1 onto a substrate made of silica nanoparticles in the air.
- the final contact angle was 0°, confirming that silicone oil 1 is stable on the silica nanoparticles.
- FIG. 9(B) shows the state after 7 seconds from dropping silicone oil 1 onto a substrate made of silica nanoparticles in water. The final contact angle was 0°, confirming that water can slide on silicone oil 1.
- compositions containing particles, binder resin, lubricating liquid, and solvent were all of the following: It was shown that a synovial surface can be formed against water by satisfying the conditions. ⁇ The lubricating liquid should show no affinity with water and show affinity with the binder resin. ⁇ The solvent should show affinity with the lubricating liquid. The final contact angle when dropped on the surface is 0 ° ⁇ The final contact angle when the lubricant is dropped on the substrate made of nanoparticles in the target liquid (here water) is 0 ° to be
- FIG. 10 is a diagram showing coatings formed from the coating compositions of Examples 10 to 12 and 15.
- FIG. 11 is a graph showing the dependence of the water contact angle and water sliding angle of the coatings formed from the coating compositions of Examples 1 and 6 to 20 on the proportion of lubricating liquid.
- FIG. 12 is a graph showing the dependence of the transmittance of the coatings formed from the coating compositions of Examples 1 and 6 to 20 on the proportion of lubricating liquid.
- the data shown by the dashed line in the figure is the transmittance of uncoated glass substrates to which no coating composition has been applied.
- the results using the coating compositions of Examples 1 and 6-20 are compared.
- the coating compositions of Examples 1 and 11-18 were found to form coatings with synovial surfaces to the liquid of interest (here water).
- coatings formed from the coating composition of Example 10 and the coating compositions of Examples 6 to 9 having a smaller lubricating liquid volume ratio (proportion) ⁇ lub did not form a sufficient liquid film, It turned out that it does not show liquidity.
- the coatings formed from the coating compositions of Examples 19 and 20 having a large volume ratio (proportion) ⁇ lub of the lubricating liquid had lower densities of the particles and the binder resin and did not exhibit synovial properties. . From this, the volume ratio (percentage) ⁇ lub of the lubricating liquid to the total amount of the solvent and lubricating liquid in the coating composition was shown to be required to satisfy the range of 0.09 or more and 0.95 or less. .
- the coating composition in which the volume ratio (proportion) ⁇ lub of the lubricating liquid is less than 0.09 corresponds to the composition of Patent Document 1.
- the water contact angle is greater than 130 °. can be formed, but even such a coating does not have water sliding property. This is because WO 2005/010000 relates to falls and the mechanism is different from the synovial surface technology.
- the volume ratio (ratio) ⁇ lub of the lubricating liquid increases, a synovial surface transparent to visible light is obtained. From this, when a transparent synovial surface is required, the volume ratio (proportion) ⁇ lub of the lubricating liquid to the total amount of the solvent and lubricating liquid in the coating composition is 0.16 or more and 0.95 or less. should satisfy the range of
- Example 1 and Examples 42-44 See Table 17 to compare the results using the coating compositions of Example 1 and Examples 42-44.
- the compositions of Examples 1 and 42 were found to form coatings with synovial surfaces to the liquid of interest (here water).
- the compositions of Examples 43 and 44 in which the binder resin content exceeded 0.05 g/mL, did not exhibit synovial properties because the binder resin hindered the fluidity of the lubricating liquid. From this, it was shown that the content of the binder resin with respect to the total amount of the lubricating liquid and the solvent must satisfy the range of 0.0004 g/mL or more and 0.05 g/mL or less.
- FIG. 13 shows SEM images of the porous underlayers of the coatings formed from the coating compositions of Examples 1 and 21-25.
- FIG. 14 shows the surface roughness of the porous underlayers of coatings formed from the coating compositions of Examples 1 and 21-25.
- the underlayer was a porous underlayer in which nanoparticles aggregated, regardless of the type and size of the particle size. Further, according to FIG. 14, the surface roughness of the porous underlayer was in the range of 0.1 ⁇ m or more and 0.25 ⁇ m or less.
- the liquid of interest here, water
- the coating compositions of Examples 1, 40, and 41 were capable of forming coatings with surfaces that were synovial to water, regardless of the particle content.
- FIG. 15 is a diagram showing the dependence of the water contact angle and water sliding angle of coatings formed from the coating compositions of Examples 1 and 21 to 25 on the surface roughness of the porous underlayer.
- FIG. 16 is a graph showing the dependence of the water contact angle and water sliding angle of coatings formed from the coating compositions of Examples 1 and 21 to 25 on the BET specific surface area of particles.
- FIG. 17 is a diagram showing the particle size (primary particle size) dependence of the water sliding angle of the films formed from the coating compositions of Examples 1 and 21-25.
- the coating compositions of Examples 1 and 21 to 29 are smooth to the target liquid (here, water). It has been found that coatings with a liquid surface can be formed.
- the coating compositions of Examples 1 and 21-29 can be used to produce a coating having a synovial surface with respect to the liquid of interest (here, water). was found to be able to form
- FIG. 18 is a diagram showing the self-healing properties of the coating formed from the coating composition of Example 1.
- Example 45 the coating composition of Example 34 was spray coated onto a glass plate and tested for synovial properties.
- the resulting film is a film comprising a porous underlayer made of hydrophobic silica nanoparticles and a liquid film made of silicone oil 2 on its surface, as described above.
- the coated glass plate was tilted, and the difference between the advancing contact angle and the receding contact angle (contact angle hysteresis) of the droplet when the droplet slid down was measured.
- the results are shown in FIG.
- FIG. 19 is a diagram showing the relationship between the contact angle hysteresis and the surface tension of the coating formed from the coating composition of Example 34 and various liquids.
- the film can repel droplets that are immiscible with silicone oil 2 regardless of the surface tension. It was also shown that, by using the coating composition of the present invention, it is possible to form a film exhibiting liquid repellency even against liquids with low surface tension, which are generally considered difficult to repel, by selecting and designing the composition. rice field.
- Example 46 the coating composition of Example 34 was spray coated onto a glass plate and tested for synovial properties in various liquids of interest.
- acetone, glycerol, and perfluoroether were used as target liquids.
- Example 34 a substrate made of silica nanoparticles of Example 34 was prepared, and the contact angle between silicone oil 2 and the substrate was examined in each target liquid. The results are shown in FIG. Next, the film formed from the coating composition of Example 34 was observed to slide down when the target liquid was dropped. The results are shown in FIG.
- FIG. 20 is a diagram showing the contact angle between the substrate made of the particles of Example 34 and the lubricating liquid.
- FIG. 20 shows the state after a predetermined time has elapsed after dropping silicone oil 2 onto a substrate made of silica nanoparticles in each target liquid.
- FIG. 20 also shows the case where the target liquid is water, as shown in FIG. 9B. It was confirmed that acetone, glycerol, and perfluoroether can slide on silicone oil 2, with the final contact angle of 0° in all cases, although there is a difference in elapsed time. Moreover, according to Table 4, it was confirmed that acetone, glycerol, and perfluoroether show no affinity with silicone oil 2.
- FIG. 21 is a diagram showing how the liquid of interest slides down on the coating formed from the coating composition of Example 34.
- Example 47 coatings formed by spray coating or dip coating the coating composition of Example 1 onto various articles were examined for water droplet slide-off.
- an aluminum plate size 300 ⁇ 300 ⁇ 0.8 mm, manufactured by Hikarisha Co., Ltd.
- a polycarbonate plate size 100 ⁇ 100 ⁇ 2.0 mm, manufactured by Takiron C.I.
- a nitrile rubber plate large (200 x 1500 x 1 mm, purchased from Nobrand Monotaro)
- a stainless steel spoon and a silicone tube (tube inner diameter 3 mm x outer diameter 5 mm, length 10 m, AS ONE Co., Ltd.) were used.
- the results are shown in FIG.
- FIG. 22 shows the synovial properties of coatings using the coating composition of Example 1 formed on various articles.
- FIG. 22 also shows the case of the glass plate shown in Example 1.
- FIG. 23 is a diagram showing changes in liquid feeding speed in a silicone tube.
- Example 48 the coating composition of Example 1 was used as a washer fluid and spray-coated on an automobile window to evaluate the synovial properties. Specifically, an automobile window was spray coated with the coating composition of Example 1, subjected to a water shower test and allowed to dry. At this time, the state of the window in each state was observed. The results are shown in FIG.
- FIG. 24 is a diagram showing the state of a shower test with and without a film on the window of an automobile.
- Example 49 coatings formed from the compositions of Examples 1 and 30-38 were tested for synovial properties in various liquids of interest.
- the coating composition was applied to a glass plate by spray coating to form a film.
- a target liquid (5 ⁇ L) was dropped on the film, and whether or not the droplets slid down was examined when the glass plate with the film was tilted at 40° and 10°. The results are shown in Table 18.
- the coating formed from the coating composition of Example 1 is synovial to water and glycerol, but synovial to acetone, oleic acid, and ethanol. do not.
- Films formed from the coating composition of Example 34 are lubricious to water, ethanol, acetone, oleic acid, polyethylene glycol, and glycerol, but are lubricious to isopropanol, hexadecane, and toluene. Not liquid.
- a lubricating liquid and a solvent it is possible to design a composition that forms a film having synovial properties against various liquids.
- the coating composition of the present invention is extremely practical because, unlike conventional coatings, a film having a synovial surface can be produced by coating.
- the coating composition of the present invention can be applied by a conventional coating method, it is possible to form a synovial surface on a desired article having an arbitrary shape.
Landscapes
- Chemical & Material Sciences (AREA)
- Organic Chemistry (AREA)
- Life Sciences & Earth Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Wood Science & Technology (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Oil, Petroleum & Natural Gas (AREA)
- Inorganic Chemistry (AREA)
- Paints Or Removers (AREA)
Abstract
Description
・表面構造が微細であるため機械耐久性が低く、指でこする程度で構造が破壊され、液滴の転落性が損なわれる。
・表面構造が光を散乱させるため、一般に透過率が低くなる。
・液体が球状になるために表面張力が作用し、このため、水よりも表面張力が低い液体を転落させることができず、特に、エタノール、アセトン、フッ素溶媒といった低表面エネルギー液体を転落させることができない。
[1]
対象とする液体に対して滑液性の表面を有する被膜のためのコーティング組成物であって、
粒子と、
前記粒子を互いに固着させるバインダ樹脂と、
前記対象とする液体とは非親和性を示し、前記バインダ樹脂とは親和性を示す潤滑液と、
前記潤滑液と親和性を示す溶媒と、を含有し、
前記潤滑液は、大気中で、前記粒子と同じ材質からなる基板上に滴下した際の接触角が0°であり、前記対象とする液体中で、前記粒子と同じ材質からなる基板上に滴下した際の接触角が0°であり、
前記溶媒及び前記潤滑液の総量に対する前記潤滑液の体積比は、0.09以上0.95以下の範囲を満たし、
前記溶媒及び前記潤滑液の総量に対する前記バインダ樹脂の含有量は、0.0004g/mL以上0.05g/mL以下の範囲を満たす、
コーティング組成物。
[2]
前記溶媒のハンセン溶解度パラメータの座標は、前記潤滑液のハンセン溶解度パラメータの座標を中心としたハンセン球内に位置し、
前記対象とする液体のハンセン溶解度パラメータの座標は、前記潤滑液のハンセン溶解度パラメータの座標を中心としたハンセン球外に位置してもよい。
[3]
前記溶媒及び前記潤滑液の総量に対する前記粒子の含有量は、0.001g/mL以上0.1g/mL以下の範囲を満たしてもよい。
[4]
前記溶媒及び前記潤滑液の総量に対する前記粒子の含有量は、0.005g/mL以上0.05g/mL以下の範囲を満たしてもよい。
[5]
前記溶媒及び前記潤滑液の総量に対する前記バインダの含有量は、0.0006g/mL以上0.03g/mL以下の範囲を満たしてもよい。
[6]
前記溶媒及び前記潤滑液の総量に対する前記潤滑液の体積比は、0.6以上0.92以下の範囲を満たしてもよい。
[7]
前記粒子の粒径は、3nm以上300nm以下の範囲を満たしてもよい。
[8]
前記粒子は、無機物、有機物、及びこれらの複合材料からなる群から選択される少なくとも一種の材料からなってもよい。
[9]
前記バインダ樹脂は、シリコーン樹脂、フッ素樹脂、エポキシ樹脂、ウレタン樹脂、オレフィン樹脂、アクリル樹脂、エチレン-酢酸ビニル共重合体(EVA)、及びポリビニルブチラール樹脂(PVB)からなる群から選択される少なくとも一種であってもよい。
[10]
前記潤滑液は、シリコーンオイル、鉱物油、植物油、動物油、重質油、樹脂、ワックス、フッ素オイル、イオン液体、及び液体金属からなる群から選択される少なくとも一種選択であってもよい。
[11]
前記溶媒は、常温常圧で揮発性を有してもよい。
[12]
前記溶媒は、水、有機溶媒、低分子液体、及びこれらの混合物からなる群から選択される少なくとも一種であってもよい。
[13]
前記対象とする液体は水であり、
前記粒子は、シリカ粒子、アルミナ粒子、チタニア粒子、及びジルコニア粒子からなる群から選択される少なくとも一種であり、
前記バインダ樹脂は、室温硬化型シリコーン樹脂であり、
前記潤滑液は、シリコーンオイル及び/又は脂肪酸であり、
前記溶媒は、イソプロパノール、ヘキサン、エタノール、アセトン、トルエン、ヘキサデカン、ジメチルスルホキシド、及びメチルエチルケトンからなる群から選択される少なくとも一種であってもよい。
[14]
対象とする液体に対して滑液性の表面を有する被膜のためのコーティング組成物の製造方法であって、
粒子と、前記粒子を互いに固着させるバインダ樹脂と、前記液体とは非親和性を示し、前記バインダ樹脂とは親和性を示す潤滑液と、前記潤滑液と親和性を示す溶媒と、を混合することを包含し、
前記潤滑液は、大気中で前記粒子と同じ材質からなる基板上に滴下した際の接触角はが0°であり、前記対象とする液体中で前記粒子と同じ材質からなる基板上に滴下した際の接触角が0°であり、
前記溶媒及び前記潤滑液の総量に対する前記溶媒の体積比は、0.09以上0.95以下の範囲を満たし、
前記溶媒及び前記潤滑液の総量に対する前記バインダ樹脂の含有量は、0.0004g/mL以上0.050g/mL以下の範囲を満たす、コーティング組成物の製造方法。
[15]
対象とする液体に対して滑液性の表面を有する被膜の製造方法であって、
上述のコーティング組成物を物品上に付与することを包含する、被膜の製造方法。
[16]
前記付与することは、浸漬コート法、フローコート法、流し塗り、カーテンコート法、スピンコート法、スプレーコート法、エアレススプレーコート法、バーコート法、ロールコート法、及び刷毛塗りからなる群から選択される少なくとも一種の手法を用いてもよい。
[17]
前記物品は、ガラス、プラスチック、ゴム、半導体、金属、カーボン、及びセラミックからなる群から選択される少なくとも一種の材料からなる表面を有してもよい。
[18]
対象とする液体に対して滑液性の表面を有する被膜を形成するための滑液性物品キットであって、
上述のコーティング組成物と、
前記コーティング組成物を用いて滑液性を有する被膜を物品上に形成する情報を伴った技術的指示書と、を備える、滑液性物品キット。
[19]
前記技術的指示書は、前記コーティング組成物を前記物品上に付与し、対象とする液体に対して滑液性の表面を有する被膜を形成することを包含してもよい。
[20]
上述のコーティング組成物を含有するウォッシャー液。
<コーティング組成物>
本発明のコーティング組成物について説明する。
粒子は、後述する図4において多孔質下地層420となるものであり、特に材質に制限はなく、所望の粒子を採用できる。粒子は、好ましくは、無機物、有機物、及びこれらの複合材料からなる群から選択される少なくとも一種の材料からなってよい。例えば、可視域において透明な被膜を得たい場合には、粒子の屈折率と潤滑液の屈折率とが近いものを選ぶとよく、粒子にとして、シリカ、ポリメチルメタクリレート、潤滑液として、シリコーンオイルを選択するとよい。
バインダ樹脂は、例示的には、シリコーン樹脂、フッ素樹脂、エポキシ樹脂、ウレタン樹脂、オレフィン樹脂、アクリル樹脂、エチレン-酢酸ビニル共重合体(EVA)、及びポリビニルブチラール樹脂(PVB)からなる群から選択される少なくとも一種であってよい。
潤滑液は、後述する図4において多孔質下地層420に含侵されるとともに、多孔質下地層上の液膜430となる。潤滑液は、対象とする液体に対しては非親和性を示し、上述のバインダ樹脂とは親和性を示す限り、特に制限はない。
溶媒は、上述の粒子、バインダ樹脂、及び潤滑液を安定に保持するよう機能し、潤滑液と親和性を示すものであれば、特に制限はない。溶媒は、好ましくは、常温常圧において揮発性を示すものがよい。これにより、通常環境下において溶媒が揮発するため、後述する図4において、本発明のコーティング組成物を単に物品に付与するだけで、1段階のコーティングプロセスにより滑液性を有する被膜を形成できる。なお、本願明細書において、「常温」とは20℃(293K)を指し、「常圧」とは1atm(絶対圧)を指す。また、常温常圧で揮発性を有する溶媒とは、20℃、1atmでの蒸気圧が10Pa未満を有する溶媒である。
ここで、潤滑液となる、シリコーンオイル、植物油としてオレイン酸、パーフルオロエーテル、石油由来の炭化水素化合物として流動オレフィン、ポリエチレングリコールに対する、代表的な溶媒/液体の親和性及び非親和性を、表4に一覧として示す。評価にあたっては、各潤滑液(0.1mL)と各溶媒/液体(0.1mL)とを混合し、よく撹拌し、5分後に二層分離又は白濁状態が見られれば、非親和性(0)を示すと判定し、二層分離及び白濁状態が見られなければ、親和性(1)を示すと判定した。表4を参照し、対象とする液体に対して、潤滑液及び溶媒を適宜選択してもよい。
[Dsol-Dlub]2+[Psol-Plub]2+[Hsol-Hlub]2<R2 (1)
[Dsol-Dlub]2+[Psol-Plub]2+[Hsol-Hlub]2>R2 (2)
ここで、Dsol、Psol、及びHsolは、それぞれ、溶媒又は液体の分散項、極性項及及び水素結合項であり、Dlub、Plub、及びHlubは、それぞれ、潤滑液の分散項、極性項、及び水素結合項であり、Rは、潤滑液のハンセン球の半径である。
図2は、表5のシリコーンオイル2のハンセン溶解度パラメータの球体を示す図である。
図3は、表5のオレイン酸のハンセン溶解度パラメータの球体を示す図である。
本発明のコーティング組成物に含まれる潤滑液は、大気中で、粒子と同じ材質からなる基板上に滴下した際の接触角が0°である。これにより、後述する図4において、粒子が多孔質下地層420を構成した際に、潤滑液からなる液膜430が多孔質下地層420上で安定となる。接触角は、JIS R 3257に準拠し、選択した潤滑液を選択した粒子と同じ材料からなる基板に滴下して測定され、十分な時間経過後の最終接触角である。このとき、評価に用いる基板は、多孔性であってもなくてもよい。
本発明のコーティング組成物は、溶媒及び潤滑液の総量に対する潤滑液の体積比が、0.09以上0.95以下の範囲を満たす。溶媒及び潤滑液の総量に対する潤滑液の体積比が0.09未満では、潤滑液が少ないため、液膜430を形成できず、滑液性を示さない。一方で、溶媒及び潤滑液の総量に対する潤滑液の体積比が0.95を超えると、潤滑液が多いため、相対的に粒子及びバインダ樹脂の割合が減り、多孔質下地層420上で潤滑液からなる皮膜が不安定となる。
本発明のコーティング組成物は、溶媒及び潤滑液の総量に対するバインダ樹脂の含有量が、0.0004g/mL以上0.05g/mL以下の範囲を満たす。溶媒及び潤滑液の総量に対するバインダ樹脂の含有量が、0.0004g/mL未満、又は0.05g/mLを超えると、バインダ樹脂の量が不適切となり、多孔質下地層420を形成できない。
本発明のコーティング組成物では、粒子の含有量に制限はないが、好ましくは、溶媒及び潤滑液の総量に対する粒子の含有量は、0.001g/mL以上0.1g/mL以下の範囲を満たす。これにより、多孔質下地層420の形成を促進できる。溶媒及び潤滑液の総量に対する粒子の含有量は、より好ましくは、0.005g/mL以上0.05g/mL以下の範囲である。この範囲であれば、良質な多孔質下地層420が形成される。溶媒及び潤滑液の総量に対する粒子の含有量は、更に好ましくは、0.005g/mL以上0.02g/mL以下の範囲である。この範囲であれば、透過率の高い多孔質下地層420となり、滑落角の小さなSLIPS被膜となる。
対象とする液体が水の場合には、本発明のコーティング組成物は、好ましくは、シリカ粒子、アルミナ粒子、チタニア粒子、及びジルコニア粒子からなる群から選択される少なくとも一種の粒子と、室温硬化型シリコーン樹脂であるバインダ樹脂と、シリコーンオイル及び/又は脂肪酸である潤滑液と、イソプロパノール、ヘキサン、エタノール、アセトン、トルエン、ヘキサデカン、ジメチルスルホキシド、及びメチルエチルケトンからなる群から選択される少なくとも一種の溶媒と、を含有するとよい。これらの組み合わせであれば、上述の条件を満たし得るため、SLIPS被膜を形成でき、水を滑落させることができる。
本発明のコーティング組成物の製造方法について説明する。
本発明のコーティング組成物の製造方法は、単に、上述の条件を満たすように、多孔質下地層を構成する粒子と、粒子を互いに固着させるバインダ樹脂と、対象とする液体に対しては非親和性を示し、バインダ樹脂とは親和性を示す潤滑液と、潤滑液と親和性を示す溶媒と、を混合するだけでよい。なお、粒子、バインダ樹脂、潤滑液、及び溶媒は、上述したとおりであるため説明を省略する。
次に、本発明のコーティング組成物を用いて、滑液性の表面を有する被膜(SLIPS被膜)を形成する方法について説明する。
物品410は、図4では簡単のため平板で示されているが、物品は平板に限らない。物品410の表面は、コーティング組成物を塗布できる限り制限はなく、例えば、曲率を有する表面であってもよいし、湾曲していてもよいし、凹凸を有していてもよい。
付与の方法は、特に制限はなく、公知の手法を用いることができ、例えば、浸漬コート法、フローコート法、流し塗り、カーテンコート法、スピンコート法、スプレーコート法、エアレススプレーコート法、バーコート法、ロールコート法、及び刷毛塗りからなる群から選択される少なくとも一種の手法を用いることができる。
本発明の滑液性物品キットは、本発明のコーティング組成物と技術的指示書とを備えるものである。
次に、本発明のコーティング組成物又は滑液性物品キットを用いた応用例を示す。
図5は、コーティング組成物を用いた滑液性の表面を有する被膜510を備えた食品容器を示す模式図である。
(1)粒子
多孔質下地層を構成する粒子として、以下を使用した。
・疎水性シリカナノ粒子1(日本アエロジル株式会社製、AEROSIL RX 200、粒径;12nm、BET比表面積;142±25m2/g)
・疎水性シリカナノ粒子2(日本アエロジル株式会社製、AEROSIL RX 50、粒径;40nm、BET比表面積;35±10m2/g)
・疎水性シリカナノ粒子3(日本アエロジル株式会社製、AEROSIL RX 300、粒径;7nm、BET比表面積;200±20m2/g)
・疎水性シリカナノ粒子4(信越化学工業株式会社製、QSG-10、粒径;14nm、BET比表面積;160m2/g)
・疎水性シリカナノ粒子5(信越化学工業株式会社製、QSG-30、粒径;40nm、BET比表面積;150m2/g)
・疎水性シリカナノ粒子6(信越化学工業株式会社製、QSG-100、粒径;117nm、BET比表面積;25m2/g)
・親水性シリカナノ粒子7(日本アエロジル株式会社製、AEROSIL OX50、粒径;40nm、BET比表面積;50±15m2/g)
・親水性シリカナノ粒子8(日本アエロジル株式会社製、AEROSIL 200、粒径;12nm、BET比表面積;200±25m2/g)
・親水性アルミナナノ粒子(日本アエロジル株式会社製、AEROXIDE Alu 65、粒径;50nm、BET比表面積;55~75m2/g)
・疎水性チタニアナノ粒子(日本アエロジル株式会社製、AEROXIDE TiO2 NKT90、粒径;14nm、BET比表面積;55~75m2/g)
バインダ樹脂として、以下を使用した。いずれも、ポリジメチルシロキサンを骨格とするシリコーン樹脂である。
・1液性室温硬化型(RTV)シリコーンゴム(ダウケミカル社製、DOWSIL(登録商標) HC 2100)
・2液性室温硬化型(RTV)シリコーンゴム(ダウケミカル社製、SYLGARD(登録商標) 184 Silicone Elastomer Kit)
溶媒、液体、又は潤滑液として、以下を使用した。
・イソプロパノール(富士フイルム和光純薬社製)
・ヘキサン(富士フイルム和光純薬社製)
・エタノール(富士フイルム和光純薬社製)
・ジクロロペンタンフルオロプロパン(AGC株式会社製、アサヒクリン(登録商標) AK-225)
・アセトン(富士フイルム和光純薬社製)
・トルエン(富士フイルム和光純薬社製)
・n-ヘキサデカン(富士フイルム和光純薬社製)
・超純水
・シリコーンオイル1(Gelest社製、DMS-T11、平均モル質量;1250g/mol、粘度;1×10-8m2/s)
・シリコーンオイル2(アズワン株式会社社製、ASO-100、粘度;1×10⁻⁴m2/s)
・オレイン酸(富士フイルム和光純薬社製)
・パーフルオロポリエーテル(Chemours社製、Krytox(登録商標) GPL-103)
・流動パラフィン(富士フイルム和光純薬社製)
・グリセリン(グリセロール)(東京化成工業社製)
・ポリエチレングリコール(富士フイルム和光純薬社製、PEG-400、数平均分子量;400)
[コーティング組成物の調製]
例1~44では、種々のコーティング組成物を調製し、それを用いた被膜を形成した。詳細には、表7~17に示す配合成分及び配合組成を満たすように、ナノ粒子、バインダ樹脂、溶媒、及び潤滑液を、それぞれ秤量し、室温(20℃)にてマグネチックスターラーにより撹拌し、コーティング組成物を調製した。
表に示すナノ粒子を板状に成形した基板を用意し、大気中又は水中で、表に示す潤滑液を滴下した際の接触角を調べた。また、バインダ樹脂からなる基板を用意し、大気中で、表に示す潤滑液を滴下した際の接触角を調べた。接触角は、接触角計(協和界面科学株式会社製、Drop master-SA-Cs1)により2θ法によって測定した。結果を図9及び表7~表17に示す。
得られたコーティング組成物をガラス板(大きさ1.0×26×76mm、武藤化学株式会社製)に付与し、被膜を作製した(図4のステップS410)。付与は、コーティング組成物をスプレーする(スプレーコート)か、又はコーティング組成物にガラス板を浸漬する(浸漬コート)かによって行った。
例1で得られた被膜の様子を、走査型電子顕微鏡(FE-SEM、株式会社日立ハイテク製、S-4800)により観察した。観察結果を図7に示す。また、例10~12、及び例14~15により得られた被膜の観察結果を、図10に示す。
得られた被膜表面に水滴5μLを滴下した際の水接触角を測定した。また、被膜表面に水滴5μLを滴下し、ガラス板を傾斜させた際の水滴の滑落角を測定した。測定結果を、図8、図11、図15~図17、及び表7~表17に示す。なお、表中「-」は、水滴が滑落しなかった場合を示す。
このようにして得られた被膜の表面に、約0.3Nで45°の角度から刃幅0.4mmのカッターで傷をつけて放置し、自己修復性を調べた。評価基準を以下に示す。評価結果を、図18、及び表7~表17に示す。
〇:傷が目視にて消失し、自己修復性有
△:傷は目視にて観察されるが、滑落角に変化はなく、自己修復性やや有
×:傷が消えず、水滴が傷部位により滑落しないため、自己修復性なし
被膜が形成されたガラス板の透過特性を分光光度計(日本分光社製、V-770)により測定した。具体的には、波長550nmにおける透過率(%)を測定した。測定結果を、図12、及び表7~表17に示す。
例1、及び例21~25で得られた被膜が形成されたガラス板に、超臨界乾燥を行い、粒子からなる多孔質下地層の状態をSEM観察し、SEM付属のエネルギー分散型X線分光法(EDX)により組成を調べた。超臨界乾燥には、超臨界乾燥装置(山友技術社製、SYGLCP-81)を用い、超臨界流体として二酸化炭素を使用した。観察結果を図13に示す。
例1、及び例21~25で得られた被膜について、レーザー顕微鏡(オリンパス社製、OLS5100)を用いて、多孔質下地層の表面粗さを測定した。表面粗さの測定結果を図14に示すとともに、表面粗さと、上記で得られた被膜の水接触角及び水滑落角との関係を図15に示す。
図8は、例1~3、及び例5のコーティング組成物から形成された被膜の水滑落角を示す図である。
・潤滑液が、水とは非親和性を示し、バインダ樹脂とは親和性を示すこと
・溶媒が潤滑液と親和性を示すこと
・大気中で、潤滑液をナノ粒子と同じ材質からなる基板上に滴下した際の最終接触角は、0°であること
・対象とする液体(ここでは水)中で、潤滑液をナノ粒子からなる基板上に滴下した際の最終接触角は、0°であること
図11は、例1、及び例6~20のコーティング組成物から形成された被膜の水接触角及び水滑落角の潤滑液の割合依存性を示す図である。
図12は、例1、及び例6~20のコーティング組成物から形成された被膜の透過率の潤滑液の割合依存性を示す図である。図中、破線で示されたデータは、コーティング組成物が適用されていない未コートのガラス基板の透過率である。
図14は、例1、及び例21~25のコーティング組成物から形成された被膜の多孔質下地層の表面粗さを示す図である。
図16は、例1、及び例21~25のコーティング組成物から形成された被膜の水接触角及び水滑落角の粒子のBET比表面積依存性を示す図である。
図17は、例1、及び例21~25のコーティング組成物から形成された被膜の水滑落角の粒子の粒径(一次粒子径)依存性を示す図である。
例45では、例34のコーティング組成物をガラス板にスプレーコートして得られた被膜の滑液性について調べた。得られた被膜は、上述したように、疎水性シリカナノ粒子からなる多孔質下地層と、その表面にシリコーンオイル2からなる液膜とを備えた膜である。
例46では、例34のコーティング組成物をガラス板にスプレーコートして得られた被膜について、種々の対象とする液体に対する滑液性について調べた。ここでは、対象とする液体としては、アセトン、グリセロール、及びパーフルオロエーテルを用いた。
例47では、例1のコーティング組成物を種々の物品にスプレーコート又は浸漬コートして形成した被膜について、水滴が滑落する様子を調べた。ここでは、物品として、アルミ板(大きさ300×300×0.8mm、株式会社光社製)、ポリカーボネート板(大きさ100×100×2.0mm、タキロンシーアイ社製)、ニトリルゴム板(大きさ200×1500×1mm、ノーブランド モノタロウで購入)、ステンレス製薬さじ、及びシリコーンチューブ(チューブ内径3mm×外径5mm、長さ10m、アズワン社製)を用いた。結果を図22に示す。
図23は、シリコーンチューブ内の送液速度の変化を示す図である。
例48では、例1のコーティング組成物をウォッシャー液として、自動車の窓にスプレーコートし、滑液性を評価した。詳細には、自動車の窓に例1のコーティング組成物をスプレーコートし、水シャワーテストを行い、乾燥させた。このとき、各状態の窓の様子を観察した。結果を図24に示す。
例49では、例1、及び例30~38の組成物から形成された被膜について、種々の対象とする液体に対する滑液性を調べた。コーティング組成物をガラス板にスプレーコートにより付与し、被膜を形成した。被膜に対象の液体(5μL)を滴下し、被膜付ガラス板を40°及び10°傾斜させた際の液滴の滑落の有無を調べた。結果を表18に示す。
420 多孔質下地層
430 液膜
440、510、610 滑液性の表面を有する被膜
Claims (20)
- 対象とする液体に対して滑液性の表面を有する被膜のためのコーティング組成物であって、
粒子と、
前記粒子を互いに固着させるバインダ樹脂と、
前記対象とする液体とは非親和性を示し、前記バインダ樹脂とは親和性を示す潤滑液と、
前記潤滑液と親和性を示す溶媒と、を含有し、
前記潤滑液は、大気中で、前記粒子と同じ材質からなる基板上に滴下した際の接触角が0°であり、前記対象とする液体中で、前記粒子と同じ材質からなる基板上に滴下した際の接触角が0°であり、
前記溶媒及び前記潤滑液の総量に対する前記潤滑液の体積比は、0.09以上0.95以下の範囲を満たし、
前記溶媒及び前記潤滑液の総量に対する前記バインダ樹脂の含有量は、0.0004g/mL以上0.05g/mL以下の範囲を満たす、
コーティング組成物。 - 前記溶媒のハンセン溶解度パラメータの座標は、前記潤滑液のハンセン溶解度パラメータの座標を中心としたハンセン球内に位置し、
前記対象とする液体のハンセン溶解度パラメータの座標は、前記潤滑液のハンセン溶解度パラメータの座標を中心としたハンセン球外に位置する、請求項1に記載のコーティング組成物。 - 前記溶媒及び前記潤滑液の総量に対する前記粒子の含有量は、0.001g/mL以上0.1g/mL以下の範囲を満たす、請求項1又は2に記載のコーティング組成物。
- 前記溶媒及び前記潤滑液の総量に対する前記粒子の含有量は、0.005g/mL以上0.05g/mL以下の範囲を満たす、請求項1又は2に記載のコーティング組成物。
- 前記溶媒及び前記潤滑液の総量に対する前記バインダの含有量は、0.0006g/mL以上0.03g/mL以下の範囲を満たす、請求項1~4のいずれかに記載のコーティング組成物。
- 前記溶媒及び前記潤滑液の総量に対する前記潤滑液の体積比は、0.6以上0.92以下の範囲を満たす、請求項1~5のいずれかに記載のコーティング組成物。
- 前記粒子の粒径は、3nm以上300nm以下の範囲を満たす、請求項1~6のいずれかに記載のコーティング組成物。
- 前記粒子は、無機物、有機物、及びこれらの複合材料からなる群から選択される少なくとも一種の材料からなる、請求項1~7のいずれかに記載のコーティング組成物。
- 前記バインダ樹脂は、シリコーン樹脂、フッ素樹脂、エポキシ樹脂、ウレタン樹脂、オレフィン樹脂、アクリル樹脂、エチレン-酢酸ビニル共重合体(EVA)、及びポリビニルブチラール樹脂(PVB)からなる群から選択される少なくとも一種である、請求項1~8のいずれかに記載のコーティング組成物。
- 前記潤滑液は、シリコーンオイル、鉱物油、植物油、動物油、重質油、樹脂、ワックス、フッ素オイル、イオン液体、及び液体金属からなる群から選択される少なくとも一種である、請求項1~9のいずれかに記載のコーティング組成物。
- 前記溶媒は、常温常圧で揮発性を有する、請求項1~10のいずれかに記載のコーティング組成物。
- 前記溶媒は、水、有機溶媒、低分子液体、及びこれらの混合物からなる群から選択される少なくとも一種である、請求項1~11のいずれかに記載のコーティング組成物。
- 前記対象とする液体は、水であり、
前記粒子は、シリカ粒子、アルミナ粒子、チタニア粒子、及びジルコニア粒子からなる群から選択される少なくとも一種であり、
前記バインダ樹脂は、室温硬化型シリコーン樹脂であり、
前記潤滑液は、シリコーンオイル及び/又は脂肪酸であり、
前記溶媒は、イソプロパノール、ヘキサン、エタノール、アセトン、トルエン、ヘキサデカン、ジメチルスルホキシド、及びメチルエチルケトンからなる群から選択される少なくとも一種である、請求項1~12のいずれかに記載のコーティング組成物。 - 対象とする液体に対して滑液性の表面を有する被膜のためのコーティング組成物の製造方法であって、
粒子と、前記粒子を互いに固着させるバインダ樹脂と、前記液体とは非親和性を示し、前記バインダ樹脂とは親和性を示す潤滑液と、前記潤滑液と親和性を示す溶媒と、を混合することを包含し、
前記潤滑液は、大気中で、前記潤滑液を前記粒子と同じ材質からなる基板上に滴下した際の接触角が0°であり、前記対象とする液体中で、前記粒子と同じ材質からなる基板上に滴下した際の接触角が0°であり、
前記溶媒及び前記潤滑液の総量に対する前記溶媒の体積比は、0.09以上0.95以下の範囲を満たし、
前記溶媒及び前記潤滑液の総量に対する前記バインダ樹脂の含有量は、0.0004g/mL以上0.050g/mL以下の範囲を満たす、コーティング組成物の製造方法。 - 対象とする液体に対して滑液性の表面を有する被膜の製造方法であって、
請求項1~13のいずれかに記載のコーティング組成物を物品上に付与することを包含する、被膜の製造方法。 - 前記付与することは、浸漬コート法、フローコート法、流し塗り、カーテンコート法、スピンコート法、スプレーコート法、エアレススプレーコート法、バーコート法、ロールコート法、及び刷毛塗りからなる群から選択される少なくとの一種の手法を用いる、請求項15に記載の製造方法。
- 前記物品は、ガラス、プラスチック、ゴム、半導体、金属、カーボン、及びセラミックからなる群から選択される少なくとも一種の材料からなる表面を有する、請求項15又は16に記載の製造方法。
- 対象とする液体に対して滑液性の表面を有する被膜を形成するための滑液性物品キットであって、
請求項1~13のいずれかに記載のコーティング組成物と、
前記コーティング組成物を用いて滑液性を有する被膜を物品上に形成する情報を伴った技術的指示書と、を備える、滑液性物品キット。 - 前記技術的指示書は、前記コーティング組成物を前記物品上に付与し、対象とする液体に対して滑液性の表面を有する被膜を形成することを包含する、請求項18に記載の滑液性物品キット。
- 請求項1~13のいずれかに記載のコーティング組成物を含有するウォッシャー液。
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP23747142.0A EP4474434A1 (en) | 2022-01-31 | 2023-01-30 | Coating composition, production method thereof, production method of coating film using same, lubricating article kit using same, and washer fluid using same |
| JP2023577068A JP7788743B2 (ja) | 2022-01-31 | 2023-01-30 | コーティング組成物、その製造方法、それを用いた被膜の製造方法、それを用いた滑液性物品キット、及びそれを用いたウォッシャー液 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2022-012495 | 2022-01-31 | ||
| JP2022012495 | 2022-01-31 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2023145932A1 true WO2023145932A1 (ja) | 2023-08-03 |
Family
ID=87471739
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2023/002857 Ceased WO2023145932A1 (ja) | 2022-01-31 | 2023-01-30 | コーティング組成物、その製造方法、それを用いた被膜の製造方法、それを用いた滑液性物品キット、及びそれを用いたウォッシャー液 |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP4474434A1 (ja) |
| JP (1) | JP7788743B2 (ja) |
| WO (1) | WO2023145932A1 (ja) |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2000104047A (ja) * | 1998-09-28 | 2000-04-11 | Soft 99 Corporation:Kk | 自動車用艶出し撥水剤組成物 |
| JP2004204131A (ja) * | 2002-12-26 | 2004-07-22 | Kao Corp | 撥水コーティング剤組成物 |
| WO2005063903A1 (ja) * | 2003-12-25 | 2005-07-14 | Snt Co., Ltd. | 撥水剤とその使用 |
| JP2018184536A (ja) * | 2017-04-26 | 2018-11-22 | 株式会社Snt | 滑落膜 |
| JP2019014793A (ja) * | 2017-07-05 | 2019-01-31 | 凸版印刷株式会社 | 撥水撥油性基材 |
| JP2020537034A (ja) * | 2017-10-16 | 2020-12-17 | ユニバーシティー オブ ヒューストン システム | 粘弾性疎氷性表面 |
-
2023
- 2023-01-30 WO PCT/JP2023/002857 patent/WO2023145932A1/ja not_active Ceased
- 2023-01-30 JP JP2023577068A patent/JP7788743B2/ja active Active
- 2023-01-30 EP EP23747142.0A patent/EP4474434A1/en active Pending
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2000104047A (ja) * | 1998-09-28 | 2000-04-11 | Soft 99 Corporation:Kk | 自動車用艶出し撥水剤組成物 |
| JP2004204131A (ja) * | 2002-12-26 | 2004-07-22 | Kao Corp | 撥水コーティング剤組成物 |
| WO2005063903A1 (ja) * | 2003-12-25 | 2005-07-14 | Snt Co., Ltd. | 撥水剤とその使用 |
| JP2018184536A (ja) * | 2017-04-26 | 2018-11-22 | 株式会社Snt | 滑落膜 |
| JP2019014793A (ja) * | 2017-07-05 | 2019-01-31 | 凸版印刷株式会社 | 撥水撥油性基材 |
| JP2020537034A (ja) * | 2017-10-16 | 2020-12-17 | ユニバーシティー オブ ヒューストン システム | 粘弾性疎氷性表面 |
Non-Patent Citations (1)
| Title |
|---|
| CHARLES M, HANSEN: "Hansen Solubility Parameters; A Users Handbook", 2007, CRC PRESS |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7788743B2 (ja) | 2025-12-19 |
| EP4474434A1 (en) | 2024-12-11 |
| JPWO2023145932A1 (ja) | 2023-08-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP7097312B2 (ja) | 液体含浸表面を利用した装置および方法 | |
| Boban et al. | Smooth, all-solid, low-hysteresis, omniphobic surfaces with enhanced mechanical durability | |
| Brown et al. | Liquid-impregnated porous polypropylene surfaces for liquid repellency | |
| Su et al. | Rational Design of Highly Comprehensive Liquid‐Like Coatings with Enhanced Transparency, Concerted Multi‐Function, and Excellent Durability: A Ternary Cooperative Strategy | |
| JP4689467B2 (ja) | 機能性皮膜被覆物品、その製造方法及び機能性皮膜形成用塗工材料 | |
| Tenjimbayashi et al. | Liquid‐infused smooth coating with transparency, super‐durability, and extraordinary hydrophobicity | |
| US11248129B2 (en) | Liquid impregnated surfaces for liquid repellancy | |
| Bhushan et al. | Substrate-independent superliquiphobic coatings for water, oil, and surfactant repellency: an overview | |
| Halvey et al. | Rapid and robust surface treatment for simultaneous solid and liquid repellency | |
| JP6171788B2 (ja) | 防汚体及びその製造方法 | |
| JP6635115B2 (ja) | 防汚構造体及びその製造方法 | |
| EP3491083B1 (en) | Compositions and methods for creating functionalized, roughened surfaces and methods of creating repellant surfaces | |
| JP6801474B2 (ja) | 撥水撥油膜 | |
| Brown et al. | Mechanically durable liquid-impregnated honeycomb surfaces | |
| Pant et al. | Enhanced slippery behavior and stability of lubricating fluid infused nanostructured surfaces | |
| JP6338702B2 (ja) | コーティング材、その製造方法、および、表面構造 | |
| US20230220173A1 (en) | Matter-repellent slippery coatings and manufacture thereof | |
| JP7788743B2 (ja) | コーティング組成物、その製造方法、それを用いた被膜の製造方法、それを用いた滑液性物品キット、及びそれを用いたウォッシャー液 | |
| JP7169048B2 (ja) | 滑落膜 | |
| Hajeesaeh et al. | Durable slippery lubricant-infused multiscale-textured surfaces for repelling highly adhesive liquids | |
| JP3426284B2 (ja) | 撥水性ガラスおよびその製造方法 | |
| Bhushan | Adaptable Fabrication Techniques for Mechanically Durable Superliquiphobic/philic Surfaces | |
| Liu | Research of Two Types of Slippery Surfaces: Slippery Polydimethylsiloxane Elastomers and Polyelectrolyte Multilayers Slippery Surfaces | |
| WO2025089219A1 (ja) | 積層体及び積層体の製造方法 | |
| Moriya et al. | Slippery-wetting materials bioinspired by pitcher plant Nepenthes rafflesiana Jack |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 23747142 Country of ref document: EP Kind code of ref document: A1 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2023577068 Country of ref document: JP |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2023747142 Country of ref document: EP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2023747142 Country of ref document: EP Effective date: 20240902 |