EP3263763B1 - Method for printing carpets - Google Patents
Method for printing carpets Download PDFInfo
- Publication number
- EP3263763B1 EP3263763B1 EP17171859.6A EP17171859A EP3263763B1 EP 3263763 B1 EP3263763 B1 EP 3263763B1 EP 17171859 A EP17171859 A EP 17171859A EP 3263763 B1 EP3263763 B1 EP 3263763B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- ink
- inks
- region
- carpet
- specific embodiment
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- D—TEXTILES; PAPER
- D06—TREATMENT OF TEXTILES OR THE LIKE; LAUNDERING; FLEXIBLE MATERIALS NOT OTHERWISE PROVIDED FOR
- D06P—DYEING OR PRINTING TEXTILES; DYEING LEATHER, FURS OR SOLID MACROMOLECULAR SUBSTANCES IN ANY FORM
- D06P5/00—Other features in dyeing or printing textiles, or dyeing leather, furs, or solid macromolecular substances in any form
- D06P5/30—Ink jet printing
-
- D—TEXTILES; PAPER
- D06—TREATMENT OF TEXTILES OR THE LIKE; LAUNDERING; FLEXIBLE MATERIALS NOT OTHERWISE PROVIDED FOR
- D06B—TREATING TEXTILE MATERIALS USING LIQUIDS, GASES OR VAPOURS
- D06B11/00—Treatment of selected parts of textile materials, e.g. partial dyeing
- D06B11/0073—Treatment of selected parts of textile materials, e.g. partial dyeing of articles
-
- D—TEXTILES; PAPER
- D06—TREATMENT OF TEXTILES OR THE LIKE; LAUNDERING; FLEXIBLE MATERIALS NOT OTHERWISE PROVIDED FOR
- D06P—DYEING OR PRINTING TEXTILES; DYEING LEATHER, FURS OR SOLID MACROMOLECULAR SUBSTANCES IN ANY FORM
- D06P1/00—General processes of dyeing or printing textiles, or general processes of dyeing leather, furs, or solid macromolecular substances in any form, classified according to the dyes, pigments, or auxiliary substances employed
- D06P1/0096—Multicolour dyeing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41J—TYPEWRITERS; SELECTIVE PRINTING MECHANISMS, i.e. MECHANISMS PRINTING OTHERWISE THAN FROM A FORME; CORRECTION OF TYPOGRAPHICAL ERRORS
- B41J3/00—Typewriters or selective printing or marking mechanisms characterised by the purpose for which they are constructed
- B41J3/407—Typewriters or selective printing or marking mechanisms characterised by the purpose for which they are constructed for marking on special material
- B41J3/4078—Printing on textile
Definitions
- a method is provided herein for applying several inks on a carpet.
- An ink typically comprises a dye and a solvent, or a dye and water.
- printing techniques for carpets can be divided into two categories: process printing and spot printing.
- each colour is built up on the carpet itself from a limited set of primary colours, for example RGB and/or CMYK.
- Inks are typically transparent, and by printing several primary colours on top of one another it is possible to produce colour combinations. To obtain a dark colour it is often even necessary to print several layers of the same primary colour on top of one another. Efficiency is relatively low in process printing.
- a separate ink is provided for each colour in a design to be printed, for example by combining several dyes manually beforehand to produce a coloured ink. Just a single colour is applied on each spot. Typically, colours are manufactured on the basis of Pantone reference numbers. The accuracy and reproducibility between different batches is relatively low in spot printing.
- the colour will still depend on factors such as the height of the carpet, orientation of the pile (direction of the pile, pile lay), glossy or matt fibres, deep-pile or low-pile carpet, loops or tufts, extruded yarn or spun yarn, thick or thin.
- separate reference numbers may exist for describing the colour US-A1-2014/212618 teaches a method for applying ink on a carpet comprising two regions.
- the invention and preferred embodiments thereof offer a solution for one or more of the above needs.
- the present invention provides a method for applying inks on a carpet, the carpet comprising at least one first region and one second region, and the method comprising the following steps:
- the second ink is also applied in a third region.
- it is carried out with a machine designed for spot printing, but wherein the first ink and the second ink are applied on top of one another in the second region as in process printing.
- the first ink and/or the second ink are applied in just one movement.
- the first ink and/or the second ink is an acid ink, preferably with a pH of at most 6.0, preferably at most 5.0, preferably at most 4.0.
- the pH values of the first ink and of the second ink are preferably equal, differing by at most 2.0, preferably at most 1.0, preferably at most 0.5.
- first ink and the second ink comprise one or more surfactants and/or dispersants, preferably as colour affine agents.
- the first and second inks are fixed after applying the second ink.
- fixing takes place by conversion of acid ink to basic ink.
- the first ink is applied before the second ink, the first ink has a viscosity that is higher than the viscosity of the second ink, and the first ink is applied with a pressure that is lower than the pressure at which the second ink is applied.
- fixing takes place through evaporation of one or more surfactants and/or dispersants.
- fixing takes place by means of steam.
- the carpet comprises a pile, wherein the pile comprises polyamide, polyacrylate, polyolefin, or cotton; and wherein the pile preferably comprises polyamide, more preferably nylon.
- the first ink and/or the second ink comprise a dye and water, and optionally one or more additives.
- the printhead moves at a speed n ⁇ v during application of the first ink and of the second ink in the second region, wherein n is equal, to within 10%, to the number of inks that are applied in the second region; and wherein preferably the difference between the flow rates at which the different inks are applied on the carpet is less than 50%, preferably less than 20%, preferably less than 10%.
- the inks are applied at a certain draw-off speed, and wherein the difference between the draw-off speeds of the different inks is less than 50%, preferably less than 20%, preferably less than 10%.
- a method for applying ink on a carpet comprising at least one first region and one second region, and the method comprising the following steps:
- the concept “hue” refers to the concept from colorimetry.
- the concept “hue” refers to the extent to which an electromagnetic stimulus that is observed by the human eye may be described as whether or not it is like red, green, blue, or yellow.
- the concept “hue” is well known in the prior art.
- the concept “hue” may for example be understood as the “hue” coordinate in the HSL (hue-saturation-lightness) colour space.
- carrier refers to a substrate that comprises a pile, the substrate being selected from the list comprising mats, carpets, and artificial grass.
- application of the first ink in the second region and application of the second ink in the second region take place simultaneously.
- the second ink is also applied in a third region. In this way, 3 different regions can already be coloured differently with 2 inks.
- the method is preferably carried out with a machine and/or inks set up for spot printing, but the first ink and the second ink are applied on top of one another just as in process printing.
- the first ink and the second ink are made up beforehand, preferably made up manually beforehand. They are preferably made up on the basis of a Pantone reference.
- the first ink and the second ink are not primary colours. Primary colours are to be understood as colour combinations such as RGB and CMYK.
- inks from spot printing in a machine designed for spot printing, it is not necessary to build up several layers of the same ink.
- the inks that are made up beforehand in spot printing are typically darker than the inks used in process printing.
- the first ink is applied in just one movement. In some embodiments the second ink is applied in just one movement. In some embodiments the first ink is applied in just one movement, and the second ink is applied in just one movement.
- a very large number of colours may thus be applied on a piece of fabric quickly and efficiently with a limited number of inks.
- inks for example just 2 movements are sufficient for 3 different colours.
- 3 inks for example just 3 movements are sufficient for 7 different colours. If some inks are applied simultaneously in one region, application can be carried out in fewer movements, and may be carried out in just 1 movement.
- the first and second inks are fixed after applying the second ink. This ensures that the first ink and the second ink can penetrate the pile well, and mix before being fixed. If the inks are each fixed individually before mixing takes place, the pile will be two-coloured instead of being of one colour.
- the term "ink” also comprises the terms colour or dye.
- cold fixation of the ink that is printed first should be avoided until all inks have been applied in that place on the substrate.
- the two inks do not mix equally, so that development of other colour mixtures depends on the specific process conditions, for example it depends on the order in which the first ink and the second ink are applied, and it depends on the amount of time that elapses between application of the first ink and of the second ink. This may not be easy to control.
- the time between application of the first ink and of the second ink depends inter alia on the position on the carpet where the inks are applied.
- an ink or a substrate may have a "+” or a "-" characteristic.
- no fixation occurs (by analogy with electric repulsion between like charges).
- fixation occurs (by analogy with electric attraction between opposite charges).
- a substrate has a "+” characteristic, and when an ink has a "-” pole, these 2 poles attract one another. Controlled application of colours on a substrate comprises the controlled occurrence of this "attraction”.
- Material properties that can be described with "+” and "-” may for example be selected from the list comprising: hydrophobicity, polarity, electric charge, acid-base character, redox character, specific pairs of reactive chemical groups, and combinations thereof.
- cold fixation is counteracted by applying a transparent ink or coating on the substrate.
- the transparent ink or coating decreases the finish of the substrate.
- the transparent ink or coating comprises ionic aids.
- colour affine agents means an additive in colorants that opposes mixing. Fixation then usually occurs as a result of a higher temperature.
- yellow affine agents means an additive in yarn that opposes mixing. Fixation then usually occurs as a result of a higher temperature.
- a "-" coating is applied on the substrate.
- the substrate When a "-" coating is applied on a substrate, the substrate also acquires a "-” characteristic. Inks that also have a “-” characteristic are then fixed less quickly on the substrate, which after treatment has also become “-”.
- the "-" coating is removed from the substrate when the substrate is heated. Through removal of the "-” coating, the substrate again acquires a "+” character, and the "-" inks are fixed on the substrate, and migrate into the substrate during fixation. For example, as a result of a temperature rise, the affine product may evaporate, so that now fixation does occur.
- a "+” coating is applied on the substrate, which preferably has a "-” characteristic. Cold fixation of inks with a "+” characteristic may be counteracted in a similar way.
- inks with a "-" characteristic are modified temporarily to display a "+" characteristic.
- this modification is achieved by altering the pH of the ink.
- the pH of an ink can be adjusted during preparation of the ink by means of an acid (e.g. citric acid) or salt (e.g. common salt) or base.
- the pH of an ink may be adjusted with acids, which are used for adjusting the viscosity of the ink (e.g. citric acid).
- Viscosity can also be modified with unblocking agents (e.g. NaOH).
- the pH of an ink can be adjusted after preparation of the ink by means of pH modifiers, such as citric acid or NaOH. The viscosity can be adjusted with a salt without altering the pH.
- the pH of an ink is adjusted by increasing the pH until the dyes in the ink become basic, in other words until the dyes in the inks are converted into their conjugated base, so that the ink acquires a "+” characteristic.
- fixation is counteracted. This ensures that different inks that are applied on the substrate successively are mixed well.
- the substrate and the inks are heated after applying the inks, the pH of the ink decreases.
- the pH of the inks decreases, they become acid again, and the inks acquire a "-” characteristic again.
- a colour typically only fixes if it is acid, and does not fix if it is basic.
- the substrate keeps its "+” characteristic, so that the mixed inks with "-” characteristic fix on the "+” substrate.
- base pigments that are tailored to one another use is made of a suitable selection of base pigments that are tailored to one another. This facilitates good mixing of the different inks.
- Base pigments that are tailored to one another e.g. RGB
- Trichromy is the colour theory whereby each colour can be reproduced on the basis of 3 primary colours.
- Base pigments with one and the same trichromy have identical "draw-off speeds". For example, for a composite colour (beige), it may be that the individual colours (red, yellow, and blue) have a different draw-off speed. For example, if red draws off more quickly, the beige will have a red sheen.
- the draw-off speeds or K-factors (K or K') differ from one another by at most 10%, preferably at most 8%, preferably at most 5%, for example at most 2%, for example at most 1%.
- the draw-off speeds or K-factors (K or K') differ from one another by at most 2.0, preferably at most 1.0, preferably at most 0.5, for example at most 0.2, for example at most 0.1.
- a first ink and a second ink are applied on a substrate, wherein the first ink has a higher viscosity than the second ink.
- a viscosity of 200 to 250 cP is used.
- the first ink has an increased viscosity of 250 to 400 cP.
- the second ink has an increased viscosity of 100 to 200 cP.
- the viscosity of the first ink is at least 10% higher than the viscosity of the second ink, preferably at least 20%, preferably at least 40%, preferably at least 50%, preferably at least 80%, preferably at least 100%, preferably at least 200%, preferably at least 300%, preferably at least 400%.
- the second ink is preferably applied on top of the first ink without mechanical aid (e.g. at a standard pressure of 1.2 bar) and with a somewhat higher pressure. In this case the second ink will "bleed out” over the first ink.
- the mechanical aid may be expressed as the pressure at which the dye is injected onto the substrate.
- the first ink is applied with a pressure of at most 1.2 bar, for example at most 1.1 bar, for example at most 1.0 bar, for example at most 0.9 bar, for example at most 0.8 bar.
- the second ink is applied with a pressure of at least 1.3 bar, for example at most 1.4 bar, for example at most 1.5 bar, for example at most 0.6 bar, for example at most 1.8 bar, for example at most 2.0 bar.
- the second ink is applied with a pressure of at least 0.1 bar more than the pressure of the first ink, for example at least 0.2 bar, for example at least 0.4 bar, for example at least 0.6 bar, for example at least 0.8 bar, for example at least 1.0 bar, for example at least 1.2 bar.
- the second ink is applied with a pressure of at least 10% higher than the pressure of the first ink, for example at least 20% higher, for example at least 40% higher, for example at least 60% higher, for example at least 80% higher, for example at least 100% higher, for example at least 120% higher.
- a first ink and a second ink are applied on a substrate, wherein the first ink has a higher viscosity then the second ink, and wherein the first ink is applied on the substrate with a somewhat lower pressure than the pressure at which the second ink is applied.
- Preferred forms are combinations as described above.
- the first ink still “lies” on the substrate.
- the second ink has a somewhat lower viscosity than the first ink, and is applied with a somewhat higher pressure than the first ink. As a result the second ink is "injected” through the first ink, into the substrate.
- the first and second inks are acid inks, preferably with a pH of at most 6.0, preferably at most 5.0, preferably at most 4.0.
- the acid inks are converted to basic inks during fixation after application.
- the basic inks have a pH of at least 8.0, preferably a pH of at least 9.0, preferably a pH of at least 10.0, preferably a pH of at least 11.0, preferably a pH of at least 12.0.
- the first ink has a pH of at least 5.5, preferably at least 6.0, preferably at least 7.0, preferably at least 8.0, preferably at least 9.0, preferably at least 10.0, preferably at least 11.0.
- the second ink has a pH of at most 5.5, preferably at most 5.0, preferably at most 4.5, preferably at most 4.0, preferably at most 3.5, preferably at most 3.0.
- the first ink has a pH that is at least 0.5 higher than the second ink, preferably at least 1.0, preferably at least 2.0, preferably at least 3.0, preferably at least 4.0, preferably at least 5.0.
- Conversion of acid inks to basic inks allows the first ink and the second ink to be mixed after applying both inks, and fixed beforehand. In this way, the pile of the second region, where both inks were applied, is nevertheless one-coloured instead of two-coloured.
- application of the colours is carried out on the basis of a pH difference, as described above. In some embodiments application of the colours is carried out on the basis of a viscosity difference, as described above. In some embodiments application of the colours is carried out on the basis of a pressure difference, as described above.
- application of the colours is carried out on the basis of a pH difference and a viscosity difference, as described above. In some embodiments application of the colours is carried out on the basis of a viscosity difference and a pressure difference, as described above. In some embodiments application of the colours is carried out on the basis of a pressure difference and a pH difference, as described above. In some embodiments application of the colours is carried out on the basis of a pH difference and a viscosity difference and a pressure difference, as described above.
- the first ink and the second ink comprise one or more surfactants (also known as surface-active substances) and/or dispersants.
- surfactants also known as surface-active substances
- dispersants are used as colour affine agents.
- a surface-active or interfacially active substance, also called tenside or surfactant (from surface-active agent) is a substance that can lower the surface tension of a liquid. A liquid with lowered surface tension can form large surfaces more easily. This has the result that the liquid forms foam more easily.
- the first ink and the second ink comprise a total amount of surfactant and dispersant from at least 0.001 g/l to at most 100.0 g/l, preferably from at least 0.01 g/l to at most 50.0 g/l, preferably from at least 0.1 g/l to at most 20.0 g/l, preferably from at least 0.2 g/l to at most 10.0 g/l, preferably from at least 0.5 g/l to at most 5.0 g/l, preferably from at least 1.0 g/l to at most 2.5 g/l.
- the one or more surfactants and/or dispersants are anionic or cationic or non-ionic surfactants and/or dispersants, preferably anionic surfactants and/or dispersants.
- the one or more surfactants and/or dispersants comprise one or more ingredients selected from the list comprising: a fatty alcohol polyglycol ether, a fatty alcohol ether phosphate, an ethoxylate, a fatty amine polyglycol ether, a sulphonate (preferably an aromatic sulphonate), an alkyl polyglycol ether, a carboxylic acid ester.
- the one or more surfactants and/or dispersants comprise an enzyme, preferably pectinase. In some embodiments the one or more surfactants and/or dispersants comprise an emulsifier. In some embodiments the one or more surfactants and/or dispersants comprise an anticrease agent. In some embodiments the one or more surfactants and/or dispersants comprise a sequestering agent.
- SARABID additives for example selected from the list comprising: SARABID 200 LL, SARABID DLO CONC, SARABID IPD, SARABID IPF, SARABID IPM, SARABID LDR, and SARABID MIP, SARABID OL, SARABID PAW, SARABID PF, SARABID SBF-N, SARABID VAT, all available from CHT Benzema.
- fixing takes place through evaporation of the one or more surfactants and/or dispersants.
- the evaporation of the surfactants and/or dispersants allows the first ink and the second ink to be fixed beforehand, to allow them to mix after application of both inks. In this way, the pile of the second region, where both inks were applied, is still one-coloured instead of two-coloured.
- Fixing preferably takes place by means of steam.
- the steam has a temperature of at least 80°C and at most 130°C, preferably at least 90°C and at most 110°C, preferably at least 95°C and at most 105°C, preferably at least 97°C and at most 99°C.
- Fixing with steam is extremely suitable for converting acid inks to basic inks.
- a carpet typically comprises pile fibres that are anchored in a backing material.
- the pile comprises polyamide, polyacrylate, polyolefin (such as polypropylene or polyethylene), or cotton. More preferably the pile comprises polyamide, most preferably nylon.
- the pile has a length from at least 1.0 mm to at most 30.0 mm, preferably from 2.0 mm to 15.0 mm, more preferably from 3.0 mm to 9.0 mm.
- the carpet is unbacked or backed, preferably unbacked.
- the carpet is preferably tufted or woven, more preferably tufted.
- the ink preferably comprises a dye and a solvent or water, more preferably a dye and water, and optionally one or more additives.
- the inks are acid inks, preferably water-based acid inks.
- the inks are acid inks, preferably water-based acid inks, and the pile comprises polyamide, preferably nylon.
- the inks are applied on the carpet in pixels.
- pixel refers to a convex part of a carpet in which one or more inks may be applied.
- a pixel is generally located in a grid of several pixels.
- the number of pixels is preferably expressed in dpi.
- the design is applied in at least 16 dpi, more preferably at least 25 dpi.
- the design is applied in at most 2400 dpi, preferably at most 1200 dpi, preferably at most 600 dpi, preferably at most 600 dpi, preferably at most 76 dpi, for example 50 dpi.
- the design is applied in at least 16 dpi and at most 2400 dpi, more preferably at least 25 dpi and at most 76 dpi.
- the characteristic size of the pixels is at least 0.01 mm, preferably at least 0.10 mm, more preferably 0.20 mm to 2.00 mm, preferably about 1.00 mm.
- a design of 40 cm x 60 cm will then have 400 x 600 pixels.
- the pixels are circular. In some embodiments the pixels are rectangular. In some embodiments the pixels are square. However, the pixels may also have other shapes.
- the characteristic size of a rectangular or square pixel is equal to the length of the diagonal of the pixel.
- the characteristic length of a circular pixel is equal to the diameter of the pixel. Similar definitions apply to pixels with other shapes.
- the method is carried out by means of a textile printer that comprises a printhead.
- the printhead may comprise X colours, with Y jets per colour.
- the printhead comprises at least 2 and at most 16 colours, preferably at least 3 and at most 12 colours, preferably at least 7 and at most 9 colours, for example 8 colours.
- each colour has at least 32 and at most 128 jets, preferably 64 jets.
- An example of a textile printer that comprises a printhead is the HSV 400 from Zimmer.
- the inks are applied by inkjet printing. This is a very efficient way of applying of inks.
- the inks are applied with a pick-up rate of at least 2.0 and at most 5.0, preferably about 3.0. With a pick-up rate of 3.0, 100g of yarn requires 300g of ink.
- the pH of the inks is the same, to within a deviation of pH value of at most 2.0, preferably at most 1.0, preferably at most 0.5
- the draw-off speed of inks may depend on their pH. In particular, acids commonly have a higher draw-off speed than bases. Thus, a similar pH of the inks may help to obtain a similar draw-off speed.
- the difference between the draw-off speeds of the different inks is less than 50%, preferably less than 10%. Preferably these percentages are expressed relative to the average of the draw-off speeds of the different inks.
- the carpet can be dyed uniformly over the thickness of the carpet. This may in particular be critical for deep-pile carpets.
- the printhead moves at a speed v during application of ink in the first region, and the printhead moves at a speed that is greater than the speed v during application of ink in the second region.
- the printhead moves at a speed n ⁇ v during application of ink in the second region, where the speed n ⁇ v is n times greater than the speed v, and where n is equal, to within 10%, to the number of inks that are applied in the second region.
- the lightness of the second region can be made to be about the same as the lightness of the first region.
- the inks have a light colour. Starting from light colours, it is possible to build up darker colours by printing different inks with light colours on top of one another. This gives designers extra freedom.
- the lightness of the ink is greater than 5, preferably greater than 7, more preferably greater than 8, when an ink is applied as a single layer on the carpet; wherein the lightness of the ink is defined according to the Munsell colour system.
- the method comprises the following step: applying the first ink, the second ink, and a third ink in a fourth region; wherein the first ink, the second ink, and the third ink each have a different hue. In this way, with 3 inks it is already possible for 7 different regions to be coloured differently.
- the method comprises the following step: applying the first ink, the second ink, a third ink, and a fourth ink in a fifth region; wherein the first ink, the second ink, the third ink, and the fourth ink each have a different hue. In this way, with 4 inks it is already possible for 15 different regions to be coloured differently.
- the difference between the flow rates at which the different inks are applied on the carpet is less than 50%, preferably less than 20%, preferably less than 10%. Preferably these percentages are expressed relative to the average flow rate at which the different inks are applied.
- Fig. 1 is a schematic representation of the width of a textile roll over a run in four different situations, in which over one run, printing is effected in a first ink with a first colour (K1), a second ink with a second colour (K2), and/or a third ink with a third colour (K3).
- a textile roll is an oblong piece of textile that comprises a longitudinal direction and a transverse direction. The textile is longer in the longitudinal direction than in the transverse direction.
- a run is a part of a textile roll and extends over the transverse direction of the textile roll. In the longitudinal direction of the textile roll the run has a width of 1 pixel.
- the textile roll is printed using a textile printer that comprises a printhead.
- a whole run is printed in ink 1 (K1).
- the printhead moves with a speed V.
- a part of the run is printed in ink 1 (K1) and a part of the run is printed in ink 2 (K2).
- the printhead also moves with a speed V.
- a part of the run is printed in ink 1 (K1), and a part of the run is printed in both ink 1 and ink 2 (K1+K2) at the same time.
- the printhead moves at a speed V.
- the printhead moves at a speed 2V.
- a part of the run is printed in ink 1 (K1), and a part of the run is printed in ink 1, ink 2, and ink 3 (K1+K2+K3) at the same time.
- the printhead moves at a speed V.
- the printhead moves at a speed 3V.
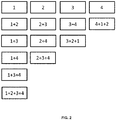
- Fig. 2 shows how a great many colours can be obtained by means of only four inks 1, 2, 3, and 4. The four inks each have a different hue.
- inks 1 to 4 can be printed individually, which already gives four possible colours. Then simultaneous printing of two inks gives six further colours (1+2, 2+3, 3+4, 1+3, 2+4, and 1+4). Furthermore, simultaneous printing of four different inks gives access to four additional colours (1+3+4, 2+3+4, 3+2+1, and 4+1+2). Finally, printing four inks together provides a final extra colour (1+2+3+4). Thus, 15 different colours can be printed with just four different inks.
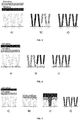
- FIG. 3, 4, and 5 illustrate a primary backing with pile, on which 2 inks are applied.
- the problem of insufficient mixing is shown schematically in FIG. 3 and 4.
- FIG. 5 shows a solution according to one embodiment of the invention.
- Steps b) and c) in FIG. 5 may for example be carried out by subjecting the first colour to a lower mechanical pressure (e.g. 1 bar) and subjecting the second colour to a higher mechanical pressure (e.g. 2 to 4 bar).
- a lower mechanical pressure e.g. 1 bar
- a higher mechanical pressure e.g. 2 to 4 bar
- the second colour penetrates mechanically through the first colour.
- This may also be effected by a viscosity difference or a pH difference (or a combination of 2 or all 3), as described above.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Materials Engineering (AREA)
- Ink Jet (AREA)
- Treatment Of Fiber Materials (AREA)
- Coloring (AREA)
- Inks, Pencil-Leads, Or Crayons (AREA)
- Ink Jet Recording Methods And Recording Media Thereof (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL17171859T PL3263763T3 (pl) | 2016-05-24 | 2017-05-19 | Sposób drukowania dywanów |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| BE2016/5381A BE1023664B1 (nl) | 2016-05-24 | 2016-05-24 | Werkwijze voor het drukken van tapijten |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3263763A1 EP3263763A1 (en) | 2018-01-03 |
| EP3263763B1 true EP3263763B1 (en) | 2018-11-28 |
Family
ID=56609609
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP17171859.6A Active EP3263763B1 (en) | 2016-05-24 | 2017-05-19 | Method for printing carpets |
Country Status (6)
| Country | Link |
|---|---|
| EP (1) | EP3263763B1 (pl) |
| BE (1) | BE1023664B1 (pl) |
| DK (1) | DK3263763T3 (pl) |
| HU (1) | HUE042741T2 (pl) |
| PL (1) | PL3263763T3 (pl) |
| TR (1) | TR201819199T4 (pl) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US12539705B2 (en) | 2023-03-06 | 2026-02-03 | Global Textile Alliance Belgium | Textured fabric printing system and method |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3969779A (en) * | 1974-07-30 | 1976-07-20 | Deering Milliken Research Corporation | Dyeing and printing of materials |
| BE904560A (fr) * | 1986-04-07 | 1986-07-31 | Barbieux Philippe | Procede d'impression de produits textiles, installation pour la mise en oeuvre de ce procede et produits imprimes grace auxdits procede et installation. |
| US6854146B2 (en) * | 2000-06-12 | 2005-02-15 | Milliken & Company | Method for producing digitally designed carpet |
| US20140212618A1 (en) * | 2013-01-30 | 2014-07-31 | Milliken & Company | Printed Textile Substrate and Process for Making |
| US9555620B2 (en) * | 2013-10-07 | 2017-01-31 | Canon Kabushiki Kaisha | Printing apparatus and method for adjusting printing position |
-
2016
- 2016-05-24 BE BE2016/5381A patent/BE1023664B1/nl not_active IP Right Cessation
-
2017
- 2017-05-19 HU HUE17171859A patent/HUE042741T2/hu unknown
- 2017-05-19 EP EP17171859.6A patent/EP3263763B1/en active Active
- 2017-05-19 DK DK17171859.6T patent/DK3263763T3/en active
- 2017-05-19 TR TR2018/19199T patent/TR201819199T4/tr unknown
- 2017-05-19 PL PL17171859T patent/PL3263763T3/pl unknown
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| BE1023664A1 (nl) | 2017-06-09 |
| BE1023664B1 (nl) | 2017-06-09 |
| TR201819199T4 (tr) | 2019-01-21 |
| PL3263763T3 (pl) | 2019-03-29 |
| DK3263763T3 (en) | 2019-03-11 |
| HUE042741T2 (hu) | 2019-07-29 |
| EP3263763A1 (en) | 2018-01-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US10619293B2 (en) | In-line digital printing system for textile materials | |
| JP6527899B2 (ja) | 捺染用インクジェットインク、インクカートリッジ、及びインクジェット捺染方法 | |
| US6357845B1 (en) | Leather coloring process, leather coloring apparatus and colored leather produced by such process | |
| CN107059279B (zh) | 簇绒地毯的连续染色方法及连续染色机 | |
| DK3263763T3 (en) | PROCEDURE FOR PRINTING CARPETS | |
| Shang | Process control in printing of textiles | |
| DE69529944T2 (de) | Textildruckverfahren sowie damit hergestellte bedruckte Textilien | |
| CN102673138B (zh) | 喷墨印染装置以及印染物的制造方法 | |
| KR101721800B1 (ko) | 원사의 다색 염색장치 및 이를 이용한 원사의 다색 염색방법 | |
| CN104047183B (zh) | 用于对织物进行染色的方法 | |
| JP2017020139A (ja) | ダイレクト昇華捺染方法 | |
| CN101688357A (zh) | 含水配料和它们用于着色或涂覆基材的用途 | |
| KR101179066B1 (ko) | 프린터 인쇄 및 붓글씨 쓰기가 가능한 기록용 원단 제조방법 및 그 기록용 원단 | |
| US20070011819A1 (en) | Method and composition for pretreating fabric for direct printing | |
| CN106854840A (zh) | 一种保证染料渗透效果的喷墨印花方法 | |
| JP2006518422A (ja) | テキスタイルの模様染色における化学薬剤の選択的な塗布 | |
| ITUB20154827A1 (it) | Procedimento per produrre un colorante, e procedimento di colorazione di tessuti. | |
| JP2004292468A (ja) | インクジェット用インク及びその製造方法及びそれを用いるインクジェット記録方法とインクジェット捺染方法 | |
| CN109551913B (zh) | 一种减少染料迁移的雪尼尔织物数码喷印工艺 | |
| JPS61231279A (ja) | 立毛布帛のインクジエツト染色方法 | |
| JP3581411B2 (ja) | 皮革加色処理方法及び加色処理装置と該加色処理装置によって製造された加色皮革 | |
| CN107354783A (zh) | 一种户外用地毯的喷墨印花工艺 | |
| US20200308430A1 (en) | Aqueous ink jet composition, method for producing aqueous ink jet composition, and method for producing recording | |
| DE2924646C2 (de) | Verfahren zum kontinuierlichen Färben einer getufteten Textilware | |
| JP2004285218A (ja) | インクジェット記録用インクセット |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20180423 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: D06P 1/00 20060101ALI20180516BHEP Ipc: D06P 5/30 20060101AFI20180516BHEP Ipc: B41J 3/407 20060101ALN20180516BHEP Ipc: D06B 11/00 20060101ALI20180516BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20180611 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1070370 Country of ref document: AT Kind code of ref document: T Effective date: 20181215 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602017001071 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 Effective date: 20190304 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190328 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190228 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190228 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190328 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190301 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: T3 Ref document number: E 29998 Country of ref document: SK |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E042741 Country of ref document: HU |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602017001071 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20190829 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190519 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200531 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: HU Payment date: 20210617 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: UEP Ref document number: 1070370 Country of ref document: AT Kind code of ref document: T Effective date: 20181128 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181128 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220520 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230314 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20230522 Year of fee payment: 7 Ref country code: DK Payment date: 20230524 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20230512 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SK Payment date: 20240515 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP Effective date: 20240531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240519 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20250521 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240519 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250521 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20250527 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20250521 Year of fee payment: 9 Ref country code: IT Payment date: 20250527 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250528 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20250522 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20250512 Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: MM4A Ref document number: E 29998 Country of ref document: SK Effective date: 20250519 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250519 |