EP3077293B1 - Verfahren und steuerung zum messen der menge eines beschichtungsfilms - Google Patents
Verfahren und steuerung zum messen der menge eines beschichtungsfilms Download PDFInfo
- Publication number
- EP3077293B1 EP3077293B1 EP14835485.5A EP14835485A EP3077293B1 EP 3077293 B1 EP3077293 B1 EP 3077293B1 EP 14835485 A EP14835485 A EP 14835485A EP 3077293 B1 EP3077293 B1 EP 3077293B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- film
- stretching
- wrapping
- controlling computer
- load
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B1/00—Packaging fluent solid material, e.g. powders, granular or loose fibrous material, loose masses of small articles, in individual containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, or jars
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B11/00—Wrapping, e.g. partially or wholly enclosing, articles or quantities of material, in strips, sheets or blanks, of flexible material
- B65B11/04—Wrapping, e.g. partially or wholly enclosing, articles or quantities of material, in strips, sheets or blanks, of flexible material the articles being rotated
- B65B11/045—Wrapping, e.g. partially or wholly enclosing, articles or quantities of material, in strips, sheets or blanks, of flexible material the articles being rotated by rotating platforms supporting the articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B11/00—Wrapping, e.g. partially or wholly enclosing, articles or quantities of material, in strips, sheets or blanks, of flexible material
- B65B11/02—Wrapping articles or quantities of material, without changing their position during the wrapping operation, e.g. in moulds with hinged folders
- B65B11/025—Wrapping articles or quantities of material, without changing their position during the wrapping operation, e.g. in moulds with hinged folders by webs revolving around stationary articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B57/00—Automatic control, checking, warning, or safety devices
- B65B57/02—Automatic control, checking, warning, or safety devices responsive to absence, presence, abnormal feed, or misplacement of binding or wrapping material, containers, or packages
- B65B57/04—Automatic control, checking, warning, or safety devices responsive to absence, presence, abnormal feed, or misplacement of binding or wrapping material, containers, or packages and operating to control, or to stop, the feed of such material, containers, or packages
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B11/00—Wrapping, e.g. partially or wholly enclosing, articles or quantities of material, in strips, sheets or blanks, of flexible material
- B65B2011/002—Prestretching mechanism in wrapping machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B2210/00—Specific aspects of the packaging machine
- B65B2210/14—Details of wrapping machines with web dispensers for application of a continuous web in layers onto the articles
- B65B2210/16—Details of wrapping machines with web dispensers for application of a continuous web in layers onto the articles the web dispenser travelling around the article along a non-rotating ring
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B2210/00—Specific aspects of the packaging machine
- B65B2210/14—Details of wrapping machines with web dispensers for application of a continuous web in layers onto the articles
- B65B2210/18—Details of wrapping machines with web dispensers for application of a continuous web in layers onto the articles the web dispenser being mounted on a rotary ring
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B2210/00—Specific aspects of the packaging machine
- B65B2210/14—Details of wrapping machines with web dispensers for application of a continuous web in layers onto the articles
- B65B2210/20—Details of wrapping machines with web dispensers for application of a continuous web in layers onto the articles the web dispenser being mounted on a rotary arm
Definitions
- the invention relates to a process for measuring quantity of film serving for wrapping loads and if desired for regulating as well the quantity of film, using an equipment as defined in the description, which equipment comprises a controlling computer.
- the secondary packing is usually a collective packaging, which clamps together several primary packing units to a package, which can be easily handled or forwarded for a person.
- the secondary packages there are generally such points of view considered that it should be lifted with two hands by a person; in accordance with the rules of work safety of the most of countries, the package should not let the goods to fall to pieces, it should protect the product even in case of unloading and reloading several times, and it should fit into the car-boot of an average car.
- the secondary package as function has another very important role that it should include such a number of product units in primary packages and in such positions that utilizes the surface of the pallet used in the given region or by the business in one layer in the best possible way.
- the dimensions of the pallets are adapted to the transportation possibilities of the region, should it be ship, plane, railroad or road transport.
- the dimensions and orientation of the secondary package units are chosen in ideal case so, that they approach the dimensions of length and width of the pallet in one layer in the best possible way from below. It is advantageous to keep the length and width of the layers formed from the secondary package units within those dimensions of the pallet, because if a package unit hangs out from the contours of the pallet, as it is highly probable that it will be damaged during the loadings on the one hand, but, on the other hand, it is worth to utilize the area on the pallet in the best possible way from the points of view both of logistics and economy.
- the secondary package should not protect the product against light, vapor or air, it is primarily destined to keep the primary packages together.
- the secondary packages usually lose their function in the trade process at the level of retail trade, where the buyers bring home the products only in primary package and the major part of the material of secondary packages is recycled. The same circulation applies to the tertiary packages, as well.
- the stretch film package applied for wrapping of lateral and/or upper surfaces of loads formed on pallets is usually tertiary package, more rarely secondary and only in extraordinary cases primary package.
- the wrapping with stretch-film, as packaging process, is usually the last technological stage in the manufacturing plants; it is destined to keep the load together and to protect it against dust, precipitation and acts against property. It has only minimal aesthetic function, it is hardly utilized as surface for advertisement. Consequently, the wrapping with stretch-film, as cost, belongs mostly to the logistics, it represents requirement rather than added value, and the quantity of film used for a load unit should be minimal, meeting the requirements of properties, density, those of primary and secondary packages of the products, as well as the quality of transport, in ideal case.
- the production plants usually know their average yearly consumption of film, regarding its distribution in time as even, or, in case of seasonal production, the film consumption can be proportional to the number of loads on the delivered pallets. It approaches the reality only in the case when the height of loads does not change. If the stretch-film wrapping machine uses a unit of film quantity to wrap a load of unit of height then it will use approximately twice as much film to wrap a load of two units of height at the same settings. Consequently, the number of loads on the delivered pallets does not give the trustworthy quantity of film used to wrap a unit of load formed on a pallet.
- the load wrapped with the shrink hood is rotated by the table and a burner nozzle fastened on a vertically moving carriage shrinks the upper and lower parts of the shrink hood circularly and the lateral part along a screw line performing a programmed movement.
- the application of the shrink hood provides appropriate protection to the load owing to the wrapping the upper part of the load.
- the disadvantage of the machine is that the shrink hood must be made previously and put onto the load.
- the manufacturing of the cap requires manual labor, in addition the specific demand of film is great, as well as the energy requirement of the shrinking is also great enough.
- the specific demand of film of the wrapping with stretchable film amounts approximately one fifth part of that of the shrink hood and the indispensable high energy requirement of the shrinking does not arise.
- the above mentioned structural units of the machines make possible that the pre-stretched film wraps the load along a screw line as result of the turning movement of the load and the vertical movement of the film.
- the stretch of the film, the overlap and the number of film windings can be changed depending on the properties of the load and the requirements of fastening.
- registration number of HUP 210302 discloses a very advantageously applicable machine enabling the stretch wrapping of loads with stretchable film also on the top surface of the load with the film applied for the wrapping of lateral surface.
- the solution ensures the perfect protection of the goods through continuity of the stretched film, rendering unnecessary putting on a shrink hood in this way.
- the essence of the machine according to the solution is that the film applied for stretch wrapping the lateral surface of the load by winding up along a screw line is led above the load and tilted from vertical position to horizontal one during the rotation of the load.
- the film is then tilted back to the vertical position during a descending movement and the wrapping of the upper part is made in this way.
- the machine according to the patent has a base frame, a table mounted in it and a mast fastened on the base frame.
- a carriage vertically moving the film is mounted on the mentioned mast and bushings are formed on the carriage.
- a shaft is inserted into the bushing and a reel of film is connected to the one end and a tilting actuator is connected to the other end of the shaft.
- a sensor for the vertical (home) position and a sensor for the horizontal position are mounted on the base frame, triggering elements mounted on the table associated to the corners of the load, as operating elements controlling the tilting.
- the disadvantage of the machine is that the stretch tension value can attain only the nearest digital value according to the step values, so it cannot be followed proportionally, consequently the tension of the film cannot be set precisely.
- the pre-stretching motor reacts faster, more accurately, with smaller redundancy to the increased tension, and the desired tension of the film can be better approached and kept during the whole time of wrapping .
- the disadvantage of the apparatus is that the quantity of the used film cannot be measured while loads of different dimensions and shapes are wrapped, and the necessary film quantity cannot be previously determined by an estimated data.
- the process is characterized by that the parameters of width, thickness and density of the film , the length of curved lateral surface perimeter of the pre-stretching roller, the ratio of pre-stretching, the slip coefficient between the film and the pre-stretching roller, the temperature of environment and the program of the foil wrapping pattern are fed into the controlling computer, then a load of arbitrary dimensions and shape is wrapped with film, the used film is removed from the load at the end of wrapping process, its mass is measured, this reference value is fed into the controlling computer, then a film wrapping is performed with a film of the same quantity and with the same pre-stretching ratio and at a nearly the same temperature of environment on a load of different dimensions and/or shape, the actually used quantity is read from the display of the controlling computer, in the cases where it is desirable to reduce or increase the quantity of film for loads of the same dimensions and/or shape, the actually desired quantity of film to be used is fed into the controlling computer and the controlling computer automatically sets the overlap of the film spiral assigned to the desired film quantity economy or to additional
- a known film-wrapping machine serves for wrapping lateral and upper parts of loading units with stretchable film. It has a base frame, a table mounted in it and a mast fastened to the base frame, to which a carriage provided with a carriage motor is fastened vertically moving a film reel, a pin is led through it a tilting pneumatic cylinder is connected to the one end and the film reel is connected to the other end of the pin, a home position sensor and a horizontal position sensor are mounted on the base frame, tilting controlling triggers arranged correspondingly to the corners of load and a base position trigger are mounted on the table, and it has a tilting film holding and pre-stretching unit fastened to the other end of the mentioned pin.
- the equipment which is not part of the invention, which can be fitted into a film-wrapping machine and having a tilting film holding and pre-stretching unit, has pre-stretching rollers provided with one or more pre-stretching motors fastened to the frame, a guiding roller containing an arm with a roller, tension setting pneumatic cylinder provided with an analogous displacement transducer and having piston provided with magnet, furthermore a pressure regulator, where the film, wound down from the film reel, is led between pre-stretching rollers, optionally connected with a gear, and one of them or the two extreme ones are driven with a pre-stretching motor or two ones, then the film is led around a guiding roller provided with a swing-arm turning around a center of rotation and having a roller, it is connected with the piston provided with magnet, mounted in the tension setting pneumatic cylinder and the piston provided with magnet is connected to the pressure regulator.
- the exterior rollers from among the pre-stretching rollers optionally complemented with leading rollers the exterior ones are provided with rotation speed transducers and with rotation speed sensors or they are provided with bearings built together with rotation speed sensors, the former ones are connected by impulse connection to a controlling computer having a display and the latter is optionally connected by impulse connection to the motor turning the table, the one of the film carriage or both to the drive of the film holding and pre-stretching unit and to the film carriage motor.
- the apparatus is applicable for the measurement of film quantity used to wrap loads having different dimensions and shapes, but it can be applied, in addition, for regulation of the film quantity after measurement, to increase or decrease the film quantity.
- the equipment can be built in a known film-wrapping machine, where the table of the film-wrapping machine is driven with a table driving motor in one of its advantageous embodiment, while the film holding and pre-stretching unit of the film wrapping equipment is provided with a drive in another advantageous embodiment.
- the quantity of used film can be calculated from the product of the perimeter of curved surface of the chosen pre-stretching roller and the number of revolutions performed during the film wrapping process, the slip coefficient between the film and the pre-stretching roller, the current pre-stretching ratio and the temperature of environment should be taken into account in order to make exact measurement.
- the difference between the rotational speeds of the pre-stretching rolls of greatest and smallest rotational speeds, either measured or previously set on the controlling computer provide data about the pre-stretching ratio.
- the controlling computer calculates greater film consumption when a greater pre-stretching ratio is chosen or set, because it compensates with a greater sliding coefficient to the greater pre-stretching ratio within the limit of elasticity.
- the actual elongation of the film will follow less and less the theoretic elongation ratio during increase of pre-stretching ratio.
- the controlling computer performs a similar compensation under influence of the temperature of environment.
- the film is stretchable in inverse proportion with the temperature of environment, but in contrary the breaking elongation is directly proportional to the temperature of environment (The film manufacturers determine the temperature limits of applicability of their products).
- the process of regulation can be performed by an apparatus wherein the pre-stretching rollers have only one pre-stretching motor and the other one or more pre-stretching rollers are connected to the motor driven roller through a gear.
- each pre-stretching roller is driven by a motor.
- the controlling computer controls the elements of the packing pattern, such as the pitch of screw line of the side wrapping, the numbers of upper lower and middle windings in quarter parts.
- the controlling computer analyzes the ratio between the existing elements and the desired economy and automatically generates the ratios between the rotational speeds of table and the film holder and pre-stretching unit or that between the film holder and pre-stretching unit and the film carriage motor necessary for the number of windings with increased pitch inversely proportional to the desired economy.
- the ratio between the overlap of winds generated by the pitch of screw-line of the film made in the wrapping cycle as starting base and the desired overlap can also be given as aimed economy, in this case the controlling computer will subtract a quantity corresponding to the ratio of the two overlaps from the quantity of the whole pattern of film-wrapping.
- the process of regulation of film quantity assigned to the film pre-stretching unit with two motors has all the advantages of the process as described at the apparatus with one motor with the completion that the apparatuses with two motors are capable to make further savings of film.
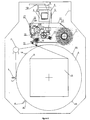
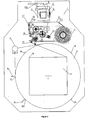
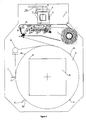
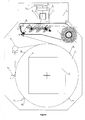
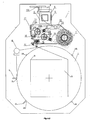
- FIGS. 1 to 4 and 9 show embodiments of the machine in top-side view wherein the table is motor-driven.
- FIGS. 5 to 8 show embodiments of the machine in top side view wherein the table does not turn but the film holding and pre-stretching unit is provided with a drive.
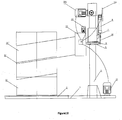
- the Figure 10 shows side view of an embodiment of the equipment.
- the Figure 1 shows an advantageous embodiment of the machine in top view, wherein the table (2) is provided with a table turning motor (21).
- a carriage (4) moving vertically the film reel (7) is fastened to the mast (3), which is fastened to the base frame (1) and bushings (5) are formed on the carriage (4).
- a pin (6) is led through the bushings (5) a tilting pneumatic cylinder (8) is connected to its one end and a film holding and pre-stretching unit (22) is connected to its other end.
- a home position sensor (9) and a 10 horizontal position sensor are arranged on the base frame (1).
- Tilting controlling triggers (12A, 12B, 12C and 12D) arranged according to the corners of load (14) and a home position sensor (9) are fitted to the table (2).
- Pre-stretching rollers (7A) provided with a pre-stretching motor (20), a guiding roller (7B) comprising a swing-arm provided with a roller (7C), a tension setting pneumatic cylinder (16) provided with a piston provided with magnet (16A) and an analogous displacement transducer (17) and a pressure regulator (18) are fastened to the frame of the film holding and pre-stretching unit (23) to the tiltable film tension setting unit (22).
- the film wound down from the film reel (7) is led around the pre-stretching rollers (7A) connected together with a gear (19), one of them is driven by the pre-stretching motor (20), then the film is led around a guiding roller (7B) provided with an swing-arm with roller (7C) turning around a center of rotation.
- the swing-arm with roller (7C) is connected to a piston provided with magnet (16A) and the piston provided with magnet (16A) is in a tension setting pneumatic cylinder (16) provided with an analogous displacement transducer (17).
- the piston provided with magnet (16A) is connected to a pressure regulator (18).
- the table (2) is driven by a table driving motor (21).
- the pre-stretching rollers (7A) of the equipment are provided with rotation speed transducers (24A, B) and rotation speed sensors (25A, B).
- the rotation speed transducers (24A, B) on the pre-stretching rollers (7A) generate an impulse in each revolution in the rotation speed transducers (24 A,B), when they reach the sensing area of the rotation speed sensors (25 A, B), which impulse is sent to the controlling computer (15).
- the quantity of film can be read from the display (15A).
- the product SM6 of the firm Bosch-Rexroth or the product named SMAT of the firm Festo are advantageously applied as analogous displacement transducer (17).
- the gear (19) can be any one of usual type, advantageously one with chain, angle belt, gearwheels, timing belt etc.
- the controlling computer changes the ratio between the speeds of rotation of the table driving motor (21) and the film carriage motor (30) (see in the Figure 10 ) and the assigned overlap of the film spiral (33).
- the Figure 2 shows another advantageous embodiment of the machine in top-side view, where the table (2) is provided with a table turning motor (21).
- This embodiment differs from the modification shown in the Figure 1 in that the pre-stretching rolls (7A) are provided not with rotation speed transducers (24A, B) and 25A, B) rotation speed sensors but they are provided with bearings built together with rotation speed sensors (26).
- the bearings built together with rotation speed sensor (26) generate several impulses depending on the construction in each revolution of a pre-stretching roller (7A).
- FIG. 3 shows a further advantageous embodiment of the machine in top-side view, wherein the table (2) is provided with a table turning motor (21).
- This embodiment differs from the one shown in the Figure 1 in that it has three pre-stretching rollers (7A) instead of two ones (7A).
- the two exterior pre-stretching rollers (7A) from the three ones are provided with rotation speed transducers (24A, B) and rotation speed sensors (25A, B).
- the film is guided between the pre-stretching rollers (7A) by leading rollers (7D).
- FIG. 4 An advantageous embodiment of the machine is shown in top-side view in the Figure 4 , wherein the table (2) is provided with a table turning motor (21).
- This embodiment differs from the one shown in the Figure 3 in that the two exterior pre-stretching rollers (7A) from those ones are equipped with bearing built together with rotation speed sensors (26) instead of rotation speed transducers (24 A, B) and rotation speed sensors (26A, B).
- a further advantageous embodiment of the machine is shown in top-side view in the Figure 5 , wherein the film holding and pre-stretching unit (22) is provided with a drive of the film holding and pre-stretching unit (27).
- This embodiment differs from the solution shown in the Figure 3 that the table (2) has not a drive.
- the drive of the film holding and pre-stretching unit (27) is a film holding driving motor with turning ring (27A).
- FIG. 6 An advantageous embodiment of the machine is shown in top-side view the Figure 6 , wherein the film holding and pre-stretching unit (22) is provided with a drive of film holding and pre-stretching unit (27).
- This embodiment differs from the one shown in the Figure 4 in that the table (2) has not a drive.
- the drive of the film holding and pre-stretching unit (27) is an arm driving motor (27B) provided with a turning arm (29).
- the turning arm (26) rotates the film.
- FIG. 7 An advantageous embodiment of the equipment is shown in top-side view in the Figure 7 , wherein the film holding and pre-stretching unit (22) is provided with a drive of the film holding and pre-stretching unit (27).
- This embodiment differs from the solution shown in the Figure 5 in that it is provided with only two pre-stretching rollers (7A) and it has no leading roller (7D).
- FIG. 8 An advantageous embodiment of the machine is shown in top-side view in the Figure 8 , wherein the film holding and pre-stretching unit (22) is provided with a drive of the film holding and pre-stretching unit (27).
- FIG. 9 An advantageous embodiment of the machine is shown in top-side view in the Figure 9 , wherein the table (2) is provided with a table turning motor (21).
- each pre-stretching roller (7A) is provided with a separate pre-stretching motor (20). So a gear (19) between the two pre-stretching rollers (7A) is not necessary. The difference between the rotation speeds of the two pre-stretching rollers (7A) determines the pre-stretching ratio.
- a carriage (4) moving vertically the film is fastened to the mast (3) fastened to the base frame (1) and bushings (5) are formed on the carriage (4).
- a pin (6) is lead through the bushings (5) and a tilting pneumatic cylinder (8) is connected to its one end and the film holding and pre-streching unit (22) is connected to its other end.
- the carriage (4) is provided with a film-carriage motor (30).
- the equipment is provided with a controlling computer (15), which is provided with a display (15A).
- the controlling computer (15) is connected by impulse connection with the pre-stretching motor (20), the table turning motor (21) and the film-carriage motor (30).
- a spirally wound up film spiral (32) is on the load (13).
- the invention relates to the process for measuring quantity of film serving for wrapping loads and if desired for regulating as well the quantity of film using the above described equipment 34A-34J.
- the advantage of the process according to the invention are as follows: The process is applicable to measure the film quantity used for wrapping loads of different dimensions and shapes, but it is applicable - if desired - at the same time for automatic reduction or increase of the film quantity by means of a computer-aided controlling regulation.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Basic Packing Technique (AREA)
- Laminated Bodies (AREA)
Claims (1)
- Ein Verfahren zur Messung der Menge des zum Einpacken eines Gepäcks benutzten Filmes und auch für Regelung der Menge des Filmes, dafür eine einen steuernden Computer (15) enthaltende Apparat benutzt wird damit gekennzeichnet dass die Parameter des Filmes d. h. die Breite die Dicke und die Dichte, die Länge der gebogenen seitlichen Oberfläche einer vorspannenden Rolle, (7A), das Maß der Vorspannung, der Koeffizient des Ausrutschens zwischen dem Film und der vorspannenden Rolle (7A), die Temperatur der Umwelt und ein Programm des Musters des Einpackens in den Film in den kontrollierenden Computer (15) eingegeben werden, dann ein Gepäck (13) der beliebigen Größe und Form wird in den Film eingepackt, die benutzte Folie wird von dem Gepäck (13) am Ende des Verpackungsverfahrens entfernt und die Menge des Filmes wird gemessen, dieser Referenzwert wird in den kontrollierenden Computer (15) eingegeben, danach eine Verpackung wird mit dem gleichen Film und mit dem gleichen Maß der Vorspannung bei der fast gleichen Temperatur der Umwelt auf einem Gepäck der unterschiedlichen Größe und/oder Form ausgeführt, die faktisch benutzte Menge des Filmes wird von dem Bildschirm (15A) des kontrollierenden Computers (15) gelesen, in den Fällen, wo eine Reduzierung oder Erhöhung der Menge des Filmes für Gepäcks der gleichen Größe und/oder Form gewünscht ist, wird die faktisch zur Benutzung erwünschte Menge des Filmes in den kontrollierenden Computer (15) eingegeben und der kontrollierende Computer (15) automatisch stellt die Überdeckung der zur Ersparnis des Filmes zugeschriebene Spirale (33) des Filmes ein oder er stellt den Apparat zur Benutzung einer zusätzlichen Menge des Filmes ein durch Abänderung die Drehzahl des den Tisch antreibenden Motors (21) und die Drehzahl einer den Film haltenden und vorspannenden Einheit (27), des den Film befördernden Motor (30) und wahlweise auch die des vorspannenden Motors (20).
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| HU1300700A HU230691B1 (hu) | 2013-12-03 | 2013-12-03 | Eljárás és berendezés tetszőleges alakú és/vagy méretű rakományok burkolására szolgáló fólia mennyiségének szabályozására |
| PCT/HU2014/000117 WO2015082945A1 (en) | 2013-12-03 | 2014-12-01 | Equipment for measuring the quantity of film for coating of loads, method and control for measuring the quantity of the coating film |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3077293A1 EP3077293A1 (de) | 2016-10-12 |
| EP3077293B1 true EP3077293B1 (de) | 2018-05-02 |
Family
ID=89991345
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP14835485.5A Active EP3077293B1 (de) | 2013-12-03 | 2014-12-01 | Verfahren und steuerung zum messen der menge eines beschichtungsfilms |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP3077293B1 (de) |
| ES (1) | ES2675147T3 (de) |
| HU (1) | HU230691B1 (de) |
| WO (1) | WO2015082945A1 (de) |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2015192250A1 (en) * | 2014-06-19 | 2015-12-23 | Crawford Packaging Inc. | Pallet wrap machine monitor |
| CN107498923B (zh) * | 2017-08-23 | 2019-04-19 | 淮安市富源包装材料有限公司 | 一种包装盒生产用的覆膜装置 |
| CN111284740B (zh) * | 2020-03-06 | 2021-08-10 | 微山县泰丰纺织有限公司 | 一种用于纱线防污隔离装置 |
| KR20250010690A (ko) * | 2022-06-03 | 2025-01-21 | 시그노드 인더스트리얼 그룹 엘엘씨 | 프리 스트레치 롤러를 구비한 스트레치 포장 기계 |
| CN116477101B (zh) * | 2023-06-21 | 2023-08-25 | 广州市鸿大胶粘制品有限公司 | 一种薄膜绕包装置 |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3633680A1 (de) | 1986-10-03 | 1988-04-14 | Dentz Verpackungsmaschinen Gmb | Vorrichtung zum schrumpfen von verpackungsfolien |
| US5524413A (en) * | 1994-02-21 | 1996-06-11 | Ishida Co., Ltd. | Packaging machine with device for monitoring remaining amount of web in a roll |
| US6370839B1 (en) * | 1999-08-10 | 2002-04-16 | Sekisui Jushi Kabushiki Kaisha | Stretch wrapping machine |
| US9908648B2 (en) * | 2008-01-07 | 2018-03-06 | Lantech.Com, Llc | Demand based wrapping |
| MX2010013053A (es) * | 2008-05-29 | 2011-07-29 | Atlantic Corp | Sistemas para monitoreo y control del consumo de materiales. |
| US8453420B2 (en) * | 2009-05-29 | 2013-06-04 | Illinois Tool Works Inc. | Film dispensing and wrapping apparatus or system using smart technology |
| EP2865600B1 (de) * | 2010-10-29 | 2016-07-13 | Lantech.Com LLC | Verfahren zur Erzeugung von Daten während der Verpackung einer Last sowie Verpackungsmaschine |
| WO2013043829A1 (en) * | 2011-09-23 | 2013-03-28 | Lantech.Com, Llc | Machine generated wrap data |
-
2013
- 2013-12-03 HU HU1300700A patent/HU230691B1/hu not_active IP Right Cessation
-
2014
- 2014-12-01 ES ES14835485.5T patent/ES2675147T3/es active Active
- 2014-12-01 WO PCT/HU2014/000117 patent/WO2015082945A1/en not_active Ceased
- 2014-12-01 EP EP14835485.5A patent/EP3077293B1/de active Active
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| WO2015082945A1 (en) | 2015-06-11 |
| ES2675147T3 (es) | 2018-07-09 |
| HU230691B1 (hu) | 2017-09-28 |
| EP3077293A1 (de) | 2016-10-12 |
| HUP1300700A2 (en) | 2015-06-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US12378029B2 (en) | Dynamic adjustment of wrap force parameter responsive to monitored wrap force and/or for film break reduction | |
| WO2015082945A1 (en) | Equipment for measuring the quantity of film for coating of loads, method and control for measuring the quantity of the coating film | |
| FI93190C (fi) | Venyvään kelmuun kääritty, kuormalavalle asetettu kuorma sekä menetelmä ja laite kuorman valmistamiseksi | |
| US11667416B2 (en) | Load wrapping apparatus wrap profiles with controlled wrap cycle interruptions | |
| AU2015330917B2 (en) | Graphical depiction of wrap profile for load wrapping apparatus | |
| CA3050578C (en) | Containment force-based wrapping | |
| EP1083126A1 (de) | Stretchfolien-Wickelvorrichtung | |
| JP4350940B2 (ja) | ストレッチ包装機 | |
| EP3049331B1 (de) | Maschine für streckverpackungslasten mit dehnfolie | |
| US11407536B2 (en) | Stretch wrapping machine with variable frequency drive torque control | |
| JPH04327108A (ja) | ストレッチ包装方法 | |
| EP2094568B1 (de) | Verfahren zum einwickeln von palletierten lasten | |
| IT202100024989A1 (it) | Metodo di fasciatura di un carico pallettizzato e relativa macchina avvolgitrice | |
| JP3586399B2 (ja) | ストレッチ包装機 | |
| EP1502855B1 (de) | Vorrichtung zum Querstrecken einer Kunststofffolie in Maschinen zum Umwickeln von palettisierten Ladungen | |
| CN213229195U (zh) | 一种钢缆生产用自动缠绕机 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20160622 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAX | Request for extension of the european patent (deleted) | ||
| 17Q | First examination report despatched |
Effective date: 20170703 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R079 Ref document number: 602014025032 Country of ref document: DE Free format text: PREVIOUS MAIN CLASS: B65B0011020000 Ipc: B65B0001000000 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B65B 11/00 20060101ALI20171129BHEP Ipc: B65B 11/04 20060101ALI20171129BHEP Ipc: B65B 57/04 20060101ALI20171129BHEP Ipc: B65B 1/00 20060101AFI20171129BHEP Ipc: B65B 11/02 20060101ALI20171129BHEP |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20180124 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: AT Ref legal event code: REF Ref document number: 994959 Country of ref document: AT Kind code of ref document: T Effective date: 20180515 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602014025032 Country of ref document: DE Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2675147 Country of ref document: ES Kind code of ref document: T3 Effective date: 20180709 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180802 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180802 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180803 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 994959 Country of ref document: AT Kind code of ref document: T Effective date: 20180502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602014025032 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20190205 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20141201 Ref country code: MK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180502 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180902 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20231214 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20231206 Year of fee payment: 10 Ref country code: LU Payment date: 20231206 Year of fee payment: 10 Ref country code: IT Payment date: 20231120 Year of fee payment: 10 Ref country code: FR Payment date: 20231206 Year of fee payment: 10 Ref country code: DE Payment date: 20231211 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20231206 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20240105 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20240102 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602014025032 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20250101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241201 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20241201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250101 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20241231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250701 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241201 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241231 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20260126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241202 |