EP3006591B1 - Verfahren zum Herstellen einer beschichteten Walze und beschichtete Walze - Google Patents
Verfahren zum Herstellen einer beschichteten Walze und beschichtete Walze Download PDFInfo
- Publication number
- EP3006591B1 EP3006591B1 EP14188479.1A EP14188479A EP3006591B1 EP 3006591 B1 EP3006591 B1 EP 3006591B1 EP 14188479 A EP14188479 A EP 14188479A EP 3006591 B1 EP3006591 B1 EP 3006591B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- base body
- ceramic material
- layer
- roller
- coating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images



Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/12—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying
- C23C4/134—Plasma spraying
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/04—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the coating material
- C23C4/10—Oxides, borides, carbides, nitrides or silicides; Mixtures thereof
- C23C4/11—Oxides
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/12—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying
- C23C4/129—Flame spraying
Definitions
- the invention relates to a method for producing a roller and a roller.
- the document DE 93 05 806 U1 relates to a method for producing a printing roller.
- a layer of copper or a copper alloy is produced on a base body made of a thermoplastic fiber-reinforced plastic by means of plasma spraying.
- US 4,997,704 A discloses a method of applying a ceramic coating to a fiber reinforced material. Before the ceramic is applied, an adhesive intermediate layer is applied to the fiber-reinforced material.
- the document EP 0 514 640 A1 discloses a method of applying a ceramic coating to a body by a thermal spraying process.
- a base body has a synthetic resin layer containing particulate material.
- the synthetic resin layer is treated before a further layer is applied by means of a thermal spraying process.
- EP 0 273 298 A2 discloses an erosion-resistant coating which adheres to a plastic with the aid of a binder.
- the document WO 2012/113426 A1 discloses a method for joining two components. During the joining, a first component made of a carbon fiber reinforced composite material is provided with a corrosion protection layer.
- the corrosion protection layer can be formed from ceramic, for example aluminum oxide.
- WO 2007/090707 A2 discloses a method for coating a substrate with at least one conductor or semiconductor layer. A metal oxide layer can be applied.
- the document DE 10 2011 120 197 A1 discloses the application of an oxide ceramic by means of thermal spraying to a core made of a fiber-reinforced material.
- the document DE 85 32 300 U1 discloses a roller tube for printing machines.
- the task is to provide improved technologies for coating components.
- a corrosion-free adhesive base for a coating is to be provided.
- a fiber-reinforced plastic (also: fiber-plastic composite or fiber composite plastic) is a material that contains reinforcing fibers that are embedded in a plastic matrix. The matrix surrounds the reinforcing fibers, which are bound to the matrix by adhesive or cohesive forces.
- the base body can for example consist of a glass fiber reinforced plastic (GRP).
- the base body can consist of a carbon fiber reinforced plastic (CFRP), a fiber reinforced polyamide (PA) or a fiber reinforced epoxy resin (EP).
- CFRP carbon fiber reinforced plastic
- PA fiber reinforced polyamide
- EP fiber reinforced epoxy resin
- the layer of ceramic material can lead to a dielectric strength of the component of up to 40 kV. Furthermore, the layer of ceramic material enables thermal insulation of the underlying body. For example, it protects against great heat.
- the layer of ceramic material is also wear-resistant, very hard, pressure-resistant and has a high layer strength.
- the layer of ceramic material can be applied to the base body in one or more layers. It can further be provided to apply several layers of different ceramic materials to the base body.
- the layer of ceramic material can be applied with a layer thickness of 100 ⁇ m to 3 mm. After curing, the layer of ceramic material can have an adhesive tensile strength of greater than or equal to 10 N / mm 2 . In another embodiment, the layer of ceramic material can have an adhesive tensile strength of greater than or equal to 5 N / mm 2 after curing.
- the base body is provided on a substrate.
- the substrate can contain a metal, for example aluminum, a metal alloy, for example steel, or a non-metal.
- the substrate can consist entirely of one of the aforementioned materials or material classes.
- the layer of ceramic material is sprayed onto the base body.
- the layer of ceramic material is applied to the base body by means of thermal spraying.
- thermal spraying filler materials, so-called spray additives, are melted, melted or melted inside or outside a spray gun.
- the filler materials are accelerated in a gas stream in the form of spray particles and onto the surface of the material to be coated Base body applied.
- a layer formation can take place here.
- Suitable thermal spray processes are, for example, high-speed flame spraying (HVOF), vacuum plasma spraying (VPS) and atmospheric plasma spraying (APS).
- Argon, hydrogen, nitrogen or a combination thereof can be used as the operating gases for atmospheric plasma spraying.
- nitrogen, a nitrogen-argon mixture, an argon-hydrogen mixture or argon can be used as the conveying gas in atmospheric plasma spraying. Cooling can be done by compressed air, carbon dioxide (CO2) or a combination thereof.
- the layer of ceramic material is formed from an oxide ceramic material, namely aluminum oxide (Al 2 O 3 ).
- the layer made of the ceramic material is applied to the base body by means of thermal spraying in powder form.
- the powder can have a degree of purity of more than 95%, preferably from 98% to 99.95%.
- the powder can be provided in the form of a powder form mentioned below: mixed ceramic material, water-atomized ceramic material, gas-atomized ceramic material, coated ceramic material, chemically coated ceramic material, agglomerated ceramic material, agglomerated and sintered ceramic material, agglomerated and hollow spherical ceramic material, agglomerated and compressed ceramic material, melted and broken ceramic , melted and broken and mixed ceramic material as well as sintered and broken ceramic material.
- Grains of the powder can have the following grain sizes: 10/5 ⁇ m, 22/5 ⁇ m, 45/16 ⁇ m, 25/5 ⁇ m, 45/20 ⁇ m and 30/10 ⁇ m. Grains of the powder can also have grain sizes in any combination of the aforementioned grain sizes. If the powder is applied to the base body by means of thermal spraying, an internal axial powder supply, an internal radial powder supply or an external powder supply can take place.
- the layer of ceramic material can be applied in the form of a suspension, for example as a water-based suspension or as an alcohol-based suspension.
- the base body can contain a resin material.
- the resin material may be, for example, an armin resin, a phenol resin, a polyester resin, a vinyl ester resin, a polyamide resin, an epoxy resin, an anhydride resin and a bismaleimite-triazine resin.
- the base body can also contain any combination of the aforementioned resins.
- the component is formed free of an electrically conductive material.
- the component can be free of metallic materials and / or metallic alloys.
- the component can be formed free of a metallic adhesive. The component can thus be formed as a corrosion-free component.
- the basic body is provided with fibers in cross layers.
- the fibers are wound in cross layers.
- the cross layers are formed with final circumferential layers.
- the base body can have a fiber content between 20 vol.% And 80 vol.%, Between 20 vol.% And 60 vol.%, Between 30 vol.% And 60 vol.% Or between 30 vol.% and have 50 vol .-%.
- the fibers can consist of glass, carbon, ceramic, plastic and / or natural fibers. Glass fibers can consist, for example, of R glass, E glass, C glass, D glass and S glass.
- the component is a rotationally symmetrical component, namely a roller with a cylindrical base body, on which a layer of ceramic material is arranged directly.
- the component can be, for example, an anilox roller or an anilox adapter or a raster sleeve for flexographic printing, a treatment roller or a treatment adapter or a treatment sleeve for a corona treatment.
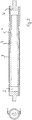
- Fig. 1 shows a schematic representation of a roller with a tubular substrate 1, a layer of a fiber-reinforced material 2 and a layer of a ceramic material 3.
- Pins 4 are arranged at both ends of the roller.
- the substrate 1 can be made of steel or aluminum, for example.
- the layer of fiber-reinforced plastic 2 serves as an insulation barrier. It can include different types of fibers, for example glass fibers, carbon fibers, ceramic fibers, plastic fibers and / or natural fibers.
- the fibers are embedded in an armin resin and applied to the tubular substrate 1 in wound cross layers.
- the layer made of a ceramic material 3 is applied directly to the fiber-reinforced layer 2.
- the ceramic layer 3 provides thermal insulation. In this embodiment, an oxide ceramic is provided as the ceramic.
- Fig. 2 shows a further embodiment of a roller.
- the tubular substrate 1 is shortened, so that an intermediate region 5 is formed between the ends of the substrate 1 and the pin 4.
- a roller with a continuous tubular substrate 1 is shown.
- Fig. 4 shows a roller with a fiber-reinforced layer 2, on which a ceramic layer 3 is arranged directly.
- the fiber-reinforced layer is applied to a substrate 6 made of a solid material, for example made of steel or aluminum.
- Fig. 5 shows a roller with a shortened tubular substrate 1, a fiber-reinforced layer 2 and a ceramic layer 3.
- a receptacle 7 is formed at both ends of the roller.
- FIGS. 6 and 7 show schematic representations for components with any shape.
- a layer of a ceramic material 8, for example of an oxide ceramic, is arranged directly on a fiber-reinforced base body 9.
- the fiber-reinforced base body 9 is arranged on a substrate 10.
- Fig. 8 shows a schematic representation of an adapter or a sleeve.
- a layer of a ceramic material 23, for example of an oxide ceramic, is arranged directly on a fiber-reinforced base sleeve 20 with a compressible intermediate layer 21 and a fiber-reinforced base body 22 built thereon.
- an intermediate layer 21 is arranged between the fiber-reinforced base body 22 and the fiber-reinforced base sleeve 20, which is formed with a compressible cover material.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Plasma & Fusion (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Rolls And Other Rotary Bodies (AREA)
- Laminated Bodies (AREA)
- Coating By Spraying Or Casting (AREA)
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL14188479T PL3006591T3 (pl) | 2014-10-10 | 2014-10-10 | Sposób wytwarzania powlekanego walca i powlekany walec |
| EP14188479.1A EP3006591B1 (de) | 2014-10-10 | 2014-10-10 | Verfahren zum Herstellen einer beschichteten Walze und beschichtete Walze |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP14188479.1A EP3006591B1 (de) | 2014-10-10 | 2014-10-10 | Verfahren zum Herstellen einer beschichteten Walze und beschichtete Walze |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3006591A1 EP3006591A1 (de) | 2016-04-13 |
| EP3006591B1 true EP3006591B1 (de) | 2019-12-25 |
Family
ID=51743281
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP14188479.1A Active EP3006591B1 (de) | 2014-10-10 | 2014-10-10 | Verfahren zum Herstellen einer beschichteten Walze und beschichtete Walze |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP3006591B1 (pl) |
| PL (1) | PL3006591T3 (pl) |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE8532300U1 (de) * | 1985-11-15 | 1986-01-02 | Felten & Guilleaume Energietechnik GmbH, 5000 Köln | Walzenrohr für Druckmaschinen mit einem auswechselbaren Mantelrohr |
| DE3644116A1 (de) | 1986-12-23 | 1988-07-07 | Mtu Muenchen Gmbh | Erosionsbestaendiger ueberzug |
| US4997704A (en) | 1989-06-02 | 1991-03-05 | Technetics Corporation | Plasma-arc ceramic coating of non-conductive surfaces |
| DE4116641A1 (de) | 1991-05-22 | 1992-11-26 | Sigri Great Lakes Carbon Gmbh | Verfahren zum beschichten eines faserverstaerkten kunststoffkoerpers |
| DE9305806U1 (de) | 1993-04-19 | 1993-06-09 | Hoechst Ag, 6230 Frankfurt | Druckwalze mit einer Hülse aus thermisch gewickelten faserverstärkten Thermoplasten und einer plasmagespritzten Kupfer- oder Kupferlegierungsbeschichtung |
| DE102006005775A1 (de) * | 2006-02-07 | 2007-08-09 | Forschungszentrum Jülich GmbH | Thermisches Spritzverfahren mit kolloidaler Suspension |
| DE102009048709B4 (de) | 2009-10-08 | 2022-11-17 | Fraunhofer-Gesellschaft zur Förderung der angewandten Forschung e.V. | Verbundbauteil aus Metall und Faserverbundwerkstoff und Verfahren zur Herstellung |
| DE102011012319A1 (de) * | 2011-02-25 | 2012-08-30 | Daimler Ag | Verfahren zum Fügen eines Bauteils aus einem faserverstärktem Verbundwerkstoff mit einem Bauteil aus einem Metall und Verbindungsanordnung solcher Bauteile |
| DE102011120197B4 (de) * | 2011-12-05 | 2015-06-18 | Technische Universität Chemnitz | Gewindespindel und Verfahren zu deren Herstellung |
-
2014
- 2014-10-10 PL PL14188479T patent/PL3006591T3/pl unknown
- 2014-10-10 EP EP14188479.1A patent/EP3006591B1/de active Active
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| PL3006591T3 (pl) | 2020-06-29 |
| EP3006591A1 (de) | 2016-04-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE60111658T2 (de) | Beschichtung auf faserverstärkte Verbundmaterialien | |
| EP1967601B1 (de) | Verfahren zur Herstellung einer Beschichtung | |
| DE9305806U1 (de) | Druckwalze mit einer Hülse aus thermisch gewickelten faserverstärkten Thermoplasten und einer plasmagespritzten Kupfer- oder Kupferlegierungsbeschichtung | |
| EP0582950A1 (de) | Faserverstärkte Kunststoffwalze mit äusserer, verschleissfester, füllerhaltiger Kunststoffschicht | |
| EP2714386B1 (de) | Verfahren zur herstellung einer oberflächenstruktur mit blitzschutz sowie damit herstellbare oberflächenstruktur | |
| EP1943369B1 (de) | Verfahren zur beschichtung eines bauteils | |
| EP3325685B1 (de) | Verfahren zur beschichtung einer zylinderlaufbahn eines zylinderkurbelgehäuses, zylinderkurbelgehäuse mit einer beschichteten zylinderlaufbahn sowie motor | |
| EP3558677B1 (de) | Verfahren zur herstellung eines verbundwerkstoff-bauteils | |
| EP0655561A1 (de) | Mit Fasern verstärkte Kunststoffwalze mit Rautierung | |
| DE69522098T2 (de) | Thermische sprühdüse zur herstellung von thermischen rauhen sprühbeschichtungen; verfahren zur herstellung von thermischen rauhen sprühbeschichtungen | |
| EP2994572B1 (de) | Walze | |
| EP1715080B1 (de) | Verfahren zur Beschichtung der inneren Oberfläche des Waffenrohres | |
| DE102008026313A1 (de) | Verfahren zur Herstellung von rohrförmigen Bauteilen aus Faserverbundwerkstoff | |
| EP1612329A1 (de) | Faserverbund Walzenbezug | |
| EP3819106B1 (de) | Verfahren zur herstellung eines verbundbauteils, das mit einem faserver-stärktem kunststoffbauteil, an dem mindestens eine oberfläche mit einer beschichtung ausgebildet ist, gebildet ist | |
| DE102018218507A1 (de) | Metallisches Wälz- oder Gleitlagerbauteil | |
| EP1593445A1 (de) | Verfahren zum Herstellen eines hohlgegossenen Bauteils mit Innenbeschichtung | |
| DE102018113587A1 (de) | Faserprofile für hohe brandschutztechnische Anforderungen und Verfahren zu ihrer Herstellung | |
| EP3006591A1 (de) | Verfahren zum Herstellen eines beschichteten Bauteils und beschichtetes Bauteil | |
| CH656560A5 (de) | Verfahren zum auftragen einer schutzschicht durch thermisches spritzen. | |
| DE102013109661A1 (de) | Verfahren zum Herstellen eines beschichteten Bauteils und beschichtetes Bauteil | |
| DE102014220337A1 (de) | Verfahren zur Herstellung eines Verbindungselements sowie Verbindungselement und CFK-Bauteil mit einem derartigen Verbindungselement | |
| EP1990444A2 (de) | Verfahren zur Nachbehandlung von Schweißverbindungen | |
| EP3362700B1 (de) | Beschichtete feder | |
| DE102004006857B4 (de) | Gradientenschicht und Verfahren zu ihrer Herstellung |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| 17P | Request for examination filed |
Effective date: 20161010 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17Q | First examination report despatched |
Effective date: 20180726 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R079 Ref document number: 502014013319 Country of ref document: DE Free format text: PREVIOUS MAIN CLASS: C23C0004100000 Ipc: C23C0004110000 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C23C 4/11 20160101AFI20190625BHEP Ipc: C23C 4/129 20160101ALI20190625BHEP Ipc: C23C 4/134 20160101ALI20190625BHEP Ipc: B41N 7/00 20060101ALI20190625BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20190718 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: INOMETA GMBH |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502014013319 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1217213 Country of ref document: AT Kind code of ref document: T Effective date: 20200115 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200325 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200325 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200326 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200425 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502014013319 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| 26N | No opposition filed |
Effective date: 20200928 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201010 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20201031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201010 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 1217213 Country of ref document: AT Kind code of ref document: T Effective date: 20201010 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201010 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191225 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20250916 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20251024 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251028 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20251023 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20251022 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20251027 Year of fee payment: 12 |