EP2550130B1 - Process for controlling the polishing process of an optical element - Google Patents
Process for controlling the polishing process of an optical element Download PDFInfo
- Publication number
- EP2550130B1 EP2550130B1 EP11706250.5A EP11706250A EP2550130B1 EP 2550130 B1 EP2550130 B1 EP 2550130B1 EP 11706250 A EP11706250 A EP 11706250A EP 2550130 B1 EP2550130 B1 EP 2550130B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- depth
- polishing
- cavities
- cavity
- reference value
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B13/00—Machines or devices designed for grinding or polishing optical surfaces on lenses or surfaces of similar shape on other work; Accessories therefor
- B24B13/0012—Machines or devices designed for grinding or polishing optical surfaces on lenses or surfaces of similar shape on other work; Accessories therefor for multifocal lenses
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B13/00—Machines or devices designed for grinding or polishing optical surfaces on lenses or surfaces of similar shape on other work; Accessories therefor
- B24B13/06—Machines or devices designed for grinding or polishing optical surfaces on lenses or surfaces of similar shape on other work; Accessories therefor grinding of lenses, the tool or work being controlled by information-carrying means, e.g. patterns, punched tapes, magnetic tapes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B49/00—Measuring or gauging equipment for controlling the feed movement of the grinding tool or work; Arrangements of indicating or measuring equipment, e.g. for indicating the start of the grinding operation
Definitions
- the invention relates to a process for controlling the polishing process of an optical element, such an ophthalmic lens.
- polishing is meaning in fact the smoothing and the polishing per se.
- the smoothing consists to suppress material on a depth comprised between 50 and 200 microns, and, after smoothing, the polishing per se consists to suppress material on a depth comprised between 3 and 50 microns.
- Ophthalmic lenses require high quality standard, therefore high quality manufacturing process is to be used in order to obtain high quality ophthalmic lenses.
- Cast molding requires the use of two complementary molds in which the lens material is added by gravity casting. These molds present a specific design corresponding to the desired lens design. Therefore, new manufacturing techniques including cutting specially digital surfacing and polishing steps are used.
- a finished lens is usually made from a semi-finished lens blank by using new technologies like digital surfacing.
- Semi-finished lens blanks have usually optically finished front surfaces. Then, they are cut, polished and coated to produce finished uncut lenses. Finished uncut lenses are then edged to the proper frontal shape and edge contour to fit into spectacle/glasses frames or other mounting structures.
- calculations are required to determine the topography of the surfaces of the lens, namely its back surface if semi-finished lens blank is used. Such calculations typically involve variables that include the front surface radii of the semi-finished blank, the index of refraction of the lens blank material, prescription values of the desired lens, statutory values regarding minimum lens thickness, and the physical dimensions of the frame or mounting structure.
- the surface is then polished and coated to produce a surface of optical quality.
- the optically finished lens is then edged to the proper shape and edge profile to fit into or with the frame for which the lens was made.
- the goal of the present invention is to provide a mechanical process for controlling the polishing process of an optical element, specially an ophthalmic lens or an ophthalmic mold, which is efficient, simple and rapid to use in workstation.
- the document US-A-6 558 586 discloses a process for measuring and/or controlling a polishing process of an ophthalmic element comprising the steps of manufacturing a cavity on the surface of the element to be polished, operating the polishing process, and considering the element, in order to check that the cavity is suppressed.
- the invention relates to a process for measuring and/or controlling a polishing process of an ophthalmic element comprising the steps of
- ophthalmic element it is understood ophthalmic lens or ophthalmic mold.
- the process for controlling a polishing process of an ophthalmic element comprises the steps of:
- two sets of cavities are manufactured, the constant depth of the first set being smaller than said reference value and the constant depth of the second set being greater than said reference value.
- a plurality of cavities can be manufactured, with different depths according to a predetermined increment.
- Said pitch is preferably comprised between 0,5 and 10 microns.
- Said cavities can be holes disposed according a regular geometric form.
- said cavities can be disposed in its near vision zone.
- Said cavities are disposed in its far vision zone.
- Said cavities are disposed in its progression corridor, between its far vision zone and its near vision zone.
- Said cavities are grooves.
- the process for measuring a polishing process of an ophthalmic element comprises the steps of:
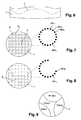
- the figure 6 is a view in vertical section of an ophthalmic element.
- Figures 7 to 9 are front views of an ophthalmic element, illustrating a process of measuring a polishing process, according to the invention.
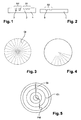
- the process for controlling a polishing process of a surfaced ophthalmic element 1 comprising the steps of:
- the reference value is comprised between 15 and 20 microns and the depth of the first holes 2 is equal to 15 microns and the depth of the second holes 3 is equal to 20 microns.
- the process of controlling permit to check that the depth of the material suppressed by polishing is effectively comprised between 15 and 20 microns. In other case, if some second holes 3 are suppressed or if some first holes 2 are always present, the polishing process presents a defect.
- the precision of the controlling can be increased by manufacturing of a plurality of holes, with different depths according to a predetermined increment, preferably comprised between 0,5 and 10 microns.
- the holes can be advantageously linear grooves, preferably disposed according a regular geometric form, for example according to concentric circles, squares or diameters. They could present specific sections, for example with form of cross, in order to be differentiated easily.
- the figure 3 illustrates such second embodiment, where the surface have a revolution symmetry and where a plurality of holes G i is manufactured according to several radius, associated to a set of constant distances to the center of the ophthalmic element, with different depths according to a predetermined increment, for example equal to 1 micron.
- the element After polishing, the element is as illustrated in the figure 4 , the present holes demonstrate that the polishing is not uniform and that the quantity of material suppressed by polishing is smaller in the vicinity of the edges of the element and higher in the vicinity of the centre of the element.
- the controlling is made in critical places of the ophthalmic element.
- the figure 5 illustrates such case of a progressive ophthalmic lens.
- the holes or the grooves can be disposed in its near vision zone and/or in its far vision zone.
- the holes or the grooves G i are disposed in the progression corridor PW, between the far zone and the near zone of the lens.
- the holes or grooves can be manufactured by means of a laser or mechanically. They can be manufactured directly in the generating or cutting machine.
- the final determination of the subsisting holes or grooves can be made by a simple visualization, by means of an arc lamp in reflective or transmissive mode or by means of a camera.
- the process according to the invention can be applied to an ophthalmic lens or to a mold to manufacture it.
- the invention concerns also a more basic process that comprises the steps of:
- this embodiment of process does not give a complete control, it can be applied in order to control the polishing in some specific cases, for example when the polishing is supposed to suppress a quantity of material too small or too great, or when the uniformity of the polishing is to control.
- the reference value X of the depth p of the material to be suppressed by polishing is not constant for one cut ophthalmic element 1 and the invention proposes for measuring a polishing in order to determine the reference surface L of polishing, as represented on the figure 6 .
- this variable depth is comprised between 50 and 200 microns for the step of smoothing and between 3 and 50 microns for the step of polishing per se.
- the process for measuring a polishing process of an ophthalmic element 1, for example in order to determine the formed reference surface L comprises the steps of:
- the process to determinate the reference surface L consists to choose some points P i on the cut element and to realise a plurality of micro-holes MH j around and in vicinity of these points.
- the number of holes is at least equal to 1 + higher natural value of maximal depth - minimal depth / increment , with maximal depth equal to 200 microns and minimal depth equal to 50 microns, for smoothing, with maximal depth equal to 50 microns and minimal depth equal to 3 microns, for polishing per se.
- Each hole of this plurality of holes has a different depth from one micron to twenty microns, with a regular increment equal to one micron.
- the element is then polished with a correct and controlled process and according to the present holes, the reference value X in said points can be defined with a precision of one micron, as illustrated on figures 8 and 9 .
- Such process can be used by repartition of each plurality of holes of different ophthalmic elements.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Grinding And Polishing Of Tertiary Curved Surfaces And Surfaces With Complex Shapes (AREA)
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP11706250.5A EP2550130B1 (en) | 2010-03-25 | 2011-03-03 | Process for controlling the polishing process of an optical element |
| PL11706250T PL2550130T3 (pl) | 2010-03-25 | 2011-03-03 | Sposób kontrolowania procesu polerowania elementu optycznego |
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP10305300 | 2010-03-25 | ||
| PCT/EP2011/053139 WO2011117050A2 (en) | 2010-03-25 | 2011-03-03 | Process for controlling the polishing process of an optical element |
| EP11706250.5A EP2550130B1 (en) | 2010-03-25 | 2011-03-03 | Process for controlling the polishing process of an optical element |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2550130A2 EP2550130A2 (en) | 2013-01-30 |
| EP2550130B1 true EP2550130B1 (en) | 2014-05-07 |
Family
ID=42537652
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP11706250.5A Active EP2550130B1 (en) | 2010-03-25 | 2011-03-03 | Process for controlling the polishing process of an optical element |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20130065489A1 (pl) |
| EP (1) | EP2550130B1 (pl) |
| CN (1) | CN103097079B (pl) |
| PL (1) | PL2550130T3 (pl) |
| PT (1) | PT2550130E (pl) |
| WO (1) | WO2011117050A2 (pl) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US9044839B2 (en) * | 2012-09-26 | 2015-06-02 | Apple Inc. | Method for measuring material removal during surface finishing on curved surfaces |
| US12622470B1 (en) * | 2024-03-12 | 2026-05-12 | CERE Creations, LLC | Breast support garment |
Family Cites Families (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1471351A (en) * | 1921-04-04 | 1923-10-23 | American Optical Corp | Lens |
| US3414272A (en) * | 1966-03-11 | 1968-12-03 | John B. Rogers Jr. | Piston rings |
| US4019289A (en) * | 1976-02-23 | 1977-04-26 | Clayton Paul Korver | Replaceable lens surfacing pad with integral wear indicating pattern |
| US5077941A (en) * | 1990-05-15 | 1992-01-07 | Space Time Analyses, Ltd. | Automatic grinding method and system |
| JP2000011327A (ja) * | 1998-06-29 | 2000-01-14 | Fujitsu Ltd | 薄膜ヘッドスライダの加工方法及び加工装置 |
| US6558586B1 (en) * | 2000-03-06 | 2003-05-06 | Essilor International (Compagnie Generale D'optique) | Process for fabricating a surface of an ophthalmic lens, installation for implementing the process and ophthalmic lens obtained by the process |
| US7008310B2 (en) * | 2001-08-01 | 2006-03-07 | Entegris, Inc. | Wafer carrier wear indicator |
| TWI252793B (en) * | 2002-08-20 | 2006-04-11 | Nanya Technology Corp | Wear auto-display polishing pad and fabricating method of the same |
| JP4105622B2 (ja) * | 2003-11-05 | 2008-06-25 | 株式会社永田製作所 | 研摩装置及び被研材の厚さ判定方法 |
| US8591716B2 (en) * | 2005-08-26 | 2013-11-26 | Panasonic Corporation | Process of making a semiconductor optical lens and a semiconductor optical lens fabricated thereby |
| US20090008794A1 (en) * | 2007-07-03 | 2009-01-08 | Weng-Jin Wu | Thickness Indicators for Wafer Thinning |
| JP2009018399A (ja) * | 2007-07-13 | 2009-01-29 | Nitta Haas Inc | 研磨パッド |
| CN100591478C (zh) * | 2008-06-16 | 2010-02-24 | 中国航空工业第一集团公司第六一三研究所 | 控制中空透镜中心厚度尺寸的方法 |
-
2011
- 2011-03-03 PL PL11706250T patent/PL2550130T3/pl unknown
- 2011-03-03 EP EP11706250.5A patent/EP2550130B1/en active Active
- 2011-03-03 PT PT117062505T patent/PT2550130E/pt unknown
- 2011-03-03 US US13/634,069 patent/US20130065489A1/en not_active Abandoned
- 2011-03-03 WO PCT/EP2011/053139 patent/WO2011117050A2/en not_active Ceased
- 2011-03-03 CN CN201180015801.XA patent/CN103097079B/zh active Active
Also Published As
| Publication number | Publication date |
|---|---|
| WO2011117050A3 (en) | 2013-02-21 |
| US20130065489A1 (en) | 2013-03-14 |
| WO2011117050A2 (en) | 2011-09-29 |
| CN103097079A (zh) | 2013-05-08 |
| PL2550130T3 (pl) | 2014-09-30 |
| CN103097079B (zh) | 2016-01-06 |
| EP2550130A2 (en) | 2013-01-30 |
| PT2550130E (pt) | 2014-07-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US10459247B2 (en) | Method for manufacturing an ophthalmic lens comprising a marking step for producing permanent technical marks on said ophthalmic lens | |
| EP2028533B1 (en) | Method of calculating an optical system according to a given spectacle frame | |
| US8721076B2 (en) | Process for controlling a lens manufacturing process | |
| CN104470680B (zh) | 加工用于制造光学镜片的未成品光学镜片构件的方法 | |
| AU2011212624B2 (en) | A method of manufacturing a lens for providing an optical display | |
| US6558586B1 (en) | Process for fabricating a surface of an ophthalmic lens, installation for implementing the process and ophthalmic lens obtained by the process | |
| US7546175B2 (en) | Method for designing mold, mold and molded product | |
| JP5691520B2 (ja) | 光学素子形成用の金型、光学素子形成用の金型の製造方法、ウエハレンズの製造方法及びウエハレンズ | |
| US9164294B2 (en) | Method for the manufacture of cost-optimized spectacle lenses | |
| CN109073913A (zh) | 用于加工未成品光学镜片构件的方法 | |
| US20130065489A1 (en) | Process for controlling the polishing process of an optical element | |
| CN105283800A (zh) | 用于确定适配于眼镜架的光学镜片的面的表面的方法 | |
| JP2000258732A (ja) | 眼鏡レンズ及びその製造方法 | |
| JP4893551B2 (ja) | セミフィニッシュトレンズブランク及びその製造方法並びに眼鏡レンズ | |
| US7832862B2 (en) | Process for the manufacture of spectacle lenses | |
| JP2016521378A (ja) | 処方レンズ作製における微細構造化眼鏡レンズの生成 | |
| CN113579316A (zh) | 超声辅助振动加工方法 | |
| JP4993999B2 (ja) | 累進屈折力眼鏡レンズ用セミフィニッシュレンズ及び累進屈折力眼鏡レンズ | |
| JP4190597B2 (ja) | 累進多焦点レンズの製造方法 | |
| EP3986709A1 (en) | A system and method for selecting an ophthalmic lens manufacturing process | |
| EP4549137A1 (en) | Method for manufacturing an optical article | |
| TWI427447B (zh) | 斜軸非球面鏡面加工系統及方法 | |
| CN110471195A (zh) | 一种远视、近视一体化眼镜及其制造方法 | |
| KR20120076028A (ko) | 누진가입도 렌즈 가공용 공구 | |
| HK1037031A (en) | Contact lenses with contoured edges |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20120917 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| R17D | Deferred search report published (corrected) |
Effective date: 20130221 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| DAX | Request for extension of the european patent (deleted) | ||
| INTG | Intention to grant announced |
Effective date: 20131126 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 666219 Country of ref document: AT Kind code of ref document: T Effective date: 20140515 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602011006787 Country of ref document: DE Effective date: 20140618 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20140708 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 666219 Country of ref document: AT Kind code of ref document: T Effective date: 20140507 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20140507 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140807 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140907 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140808 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602011006787 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20150210 |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E022192 Country of ref document: HU |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602011006787 Country of ref document: DE Effective date: 20150210 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150303 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150331 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150303 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150331 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: FH1C Free format text: FORMER REPRESENTATIVE(S): MESZAROSNE DONUSZ KATALIN, SBGK SZABADALMI UEGYVIVOEI IRODA, HU Representative=s name: SBGK SZABADALMI UEGYVIVOEI IRODA, HU Ref country code: HU Ref legal event code: GB9C Owner name: ESSILOR INTERNATIONAL, FR Free format text: FORMER OWNER(S): ESSILOR INTERNATIONAL (COMPAGNIE GENERALE D'OPTIQUE), FR |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 602011006787 Country of ref document: DE Owner name: ESSILOR INTERNATIONAL, FR Free format text: FORMER OWNER: ESSILOR INTERNATIONAL (COMPAGNIE GENERALE D'OPTIQUE), CHARENTON-LE-PONT, FR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP Owner name: ESSILOR INTERNATIONAL, FR Effective date: 20180601 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140507 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230525 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20260327 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20260327 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20260319 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: HU Payment date: 20260225 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20260325 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PT Payment date: 20260224 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20260220 Year of fee payment: 16 |