EP2474665B1 - Yankee-Zylinder für eine Tissue-Papiermaschine - Google Patents
Yankee-Zylinder für eine Tissue-Papiermaschine Download PDFInfo
- Publication number
- EP2474665B1 EP2474665B1 EP12150696.8A EP12150696A EP2474665B1 EP 2474665 B1 EP2474665 B1 EP 2474665B1 EP 12150696 A EP12150696 A EP 12150696A EP 2474665 B1 EP2474665 B1 EP 2474665B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- roller body
- yankee cylinder
- cylinder according
- hard material
- layer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 239000000463 material Substances 0.000 claims description 31
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims description 23
- 229910002804 graphite Inorganic materials 0.000 claims description 23
- 239000010439 graphite Substances 0.000 claims description 23
- 229910001018 Cast iron Inorganic materials 0.000 claims description 14
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims description 8
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 7
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 claims description 4
- 229910010293 ceramic material Inorganic materials 0.000 claims description 4
- 229910052804 chromium Inorganic materials 0.000 claims description 4
- 239000011651 chromium Substances 0.000 claims description 4
- 238000010285 flame spraying Methods 0.000 claims description 4
- 229910052759 nickel Inorganic materials 0.000 claims description 4
- 238000007750 plasma spraying Methods 0.000 claims description 4
- 150000001875 compounds Chemical class 0.000 claims description 3
- UONOETXJSWQNOL-UHFFFAOYSA-N tungsten carbide Chemical compound [W+]#[C-] UONOETXJSWQNOL-UHFFFAOYSA-N 0.000 claims description 2
- 238000001035 drying Methods 0.000 description 16
- 238000005266 casting Methods 0.000 description 6
- 230000002093 peripheral effect Effects 0.000 description 6
- 229910001060 Gray iron Inorganic materials 0.000 description 5
- 238000001816 cooling Methods 0.000 description 4
- 239000011449 brick Substances 0.000 description 3
- 238000000576 coating method Methods 0.000 description 3
- 238000004519 manufacturing process Methods 0.000 description 3
- HBMJWWWQQXIZIP-UHFFFAOYSA-N silicon carbide Chemical compound [Si+]#[C-] HBMJWWWQQXIZIP-UHFFFAOYSA-N 0.000 description 3
- 229910010271 silicon carbide Inorganic materials 0.000 description 3
- 125000006850 spacer group Chemical group 0.000 description 3
- 229910001141 Ductile iron Inorganic materials 0.000 description 2
- 239000011248 coating agent Substances 0.000 description 2
- 229910052751 metal Inorganic materials 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 239000007787 solid Substances 0.000 description 2
- 239000010959 steel Substances 0.000 description 2
- 229910001208 Crucible steel Inorganic materials 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- 230000002745 absorbent Effects 0.000 description 1
- 239000002250 absorbent Substances 0.000 description 1
- 229910052799 carbon Inorganic materials 0.000 description 1
- 229920002678 cellulose Polymers 0.000 description 1
- 239000001913 cellulose Substances 0.000 description 1
- 238000005253 cladding Methods 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
- 239000002657 fibrous material Substances 0.000 description 1
- 239000002054 inoculum Substances 0.000 description 1
- 229910001105 martensitic stainless steel Inorganic materials 0.000 description 1
- 239000000155 melt Substances 0.000 description 1
- 238000001556 precipitation Methods 0.000 description 1
- 229910052710 silicon Inorganic materials 0.000 description 1
- 238000004381 surface treatment Methods 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
Images
Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F5/00—Dryer section of machines for making continuous webs of paper
- D21F5/02—Drying on cylinders
- D21F5/021—Construction of the cylinders
Definitions
- the invention relates to a Yankee cylinder for a tissue paper machine.
- Drying cylinders for tissue paper machines usually have a hollow roll body, which is poured for usually gray-solidifying cast iron with lamellar graphite.
- the roll body can also be produced by welding steel sheet.
- the hollow cast iron body is usually subjected to a water vapor pressure of about 10 bar.
- Such drying cylinders are used in the dewatering of fibrous materials (tissue material) from which, for example, paper or cellulose products such as absorbent and soft kitchen towels, toilet paper, baby diapers, crepe paper or the like is produced.
- fibrous materials tissue material
- a so-called doctor blade abuts on the outer circumferential surface of the roll body, whereby the paper is stripped and crimped from the peripheral surface of the cylinder.
- a hard material layer may be provided on the outer peripheral surface of the roller body.
- a hard material layer is understood as meaning a layer of a hard material which has a greater hardness than the material of the roller body.
- a Yankee cylinder and a method for coating a Yankee cylinder are described.
- the cladding coating is applied directly to the surface of the shell, which is made of cast iron or steel.
- an intermediate layer of a martensitic stainless steel is first applied to the mantle surface of the Yankee cylinder, which is then again coated again.
- the roller has a metal core or metal body on which a relatively soft inner layer and a relatively hard outer layer are applied. Both the inner and outer layers are made of solid rubber.
- the object of the invention is to provide a coated drying cylinder with improved dry properties for a tissue paper machine, which can be produced inexpensively and procedurally simple.
- a drying cylinder for a tissue paper machine in particular a Yankee cylinder, comprises a hollow roll body of gray cast iron (GJS) with freely embedded graphite, which is present at least substantially as spheroidal graphite, wherein on a outer peripheral surface of the roll body a hard material layer is applied.
- GJS gray cast iron
- the cast structure of the roller body is advantageously also in its radially outer region predominantly, preferably at least substantially gray, so solidified solid.
- Gray solidified cast iron with free embedded graphite advantageously has a higher thermal conductivity than white solidified cast iron, whereby the dry properties of the drying cylinder can be improved.
- the drying process can thus be made more energy-efficient, that is cheaper and more environmentally friendly.
- Gray cast iron can also be better worked than white, in particular, including boring.
- the roll body may have a diameter of at least 1.5 m and preferably at most 7 m, preferably at least 4 m and preferably at most 6 m.
- the roll body may have a length of at least 2 m and preferred not more than 9 m, preferably of at least 4 m and advantageously not more than 7 m.
- the roll body can have a shell thickness of at least 20 mm and preferably at most 150 mm, preferably at least 40 mm and in particular at most 100 mm.
- the roller body can form a pressure vessel, which can be acted upon by a pressure, in particular a water vapor pressure, of preferably up to 15 bar.
- the shell thickness of the roll body can be adapted to the water vapor pressure to be resisted in order to comply with legal requirements for pressure vessels.
- At least one rib in particular a circumferential rib may be arranged on an inner surface of the roller body.
- Such ribs provide greater heat transfer and at the same time for a stiffening of the roll body.
- a plurality of ribs in particular at the same distance from one another, are arranged on the inner surface of the roller body.
- an inner cylinder preferably coaxially, can be arranged as a so-called displacer within the roller body.
- At least one spacer element can be provided between an inner surface of the roller body and an outer surface of the inner cylinder.
- a plurality of spacers are provided as axial ribs between the inner surface of the roll body and the outer surface of the inner cylinder, whereby both the heat transfer and the rigidity of the roll body can be improved.
- the roll body is produced by casting against silicon carbide bricks, preferably in a casting of silicon carbide bricks.
- the cooling rate of the cast body can be adjusted so that the melt solidifies gray even in the peripheral edge zone of the roll body.
- the gray-solidified cast iron of the roll body can have a saturation degree S c of at least 0.8 and at most 1.1, preferably of at least 0.96 and at most 1.003.
- the graphite spheres of spheroidal graphite have an average diameter of at least 0.01 mm and at most 0.1 mm, preferably of at least 0.02 and at most 0.04 mm.
- the precipitation of the graphite in the form of only such small graphite balls is advantageous for the mechanical strength and can be achieved in the casting process by adding seed elements. By a targeted adjustment of the cooling rate, the size of the graphite balls can be controlled.
- Spheroidal Graphite Cast Iron has higher strength and higher elongation than cast iron with lamellar graphite (GJL). For this reason, the safety factor for spheroidal graphite cast iron (GJS) is lower, so that lower shell thickness of the roll body can be implemented. Lower jacket thicknesses in turn lead to a lower mass moment of inertia of the drying cylinder, resulting in a more favorable energy balance.
- the proportion of spheroidal graphite on freely stored graphite at least 80 wt.%, Preferably at least 90 wt.%, Amount.
- the hard material layer may have a thickness of at least 0.01 mm and preferably at most 1 mm, preferably at least 0.1 mm and in particular at most 0.5 mm.
- the hard material layer may comprise a ceramic material, preferably tungsten carbide, or nickel or chromium.
- the word "or” is understood in the usual logical sense and therefore as an “inclusive or”, thus includes both the meaning of "either ... or” as well as the meaning of "and”, as far as the respective concrete context exclusively opens only a limited meaning.
- the hard material layer may comprise a ceramic material, nickel or chromium as a single compound or more of these materials in combination.
- the hard material layer can be applied by means of flame spraying or plasma spraying.
- Flame or plasma spraying are procedural suitable surface treatments with which articles of different geometry and dimensions can be coated. Especially for a very large-sized roll body, these coating methods have been found to be advantageous.
- hard material can be deposited galvanically, electrolytically or autocatalytically on the outer circumferential surface of the roller body.
- the hollow roll body is made by casting cast iron.
- silicon carbide bricks or other cooling materials may be used.
- the casting parameters, such. Thickness of the mold, mold material, inoculant, as well as the cooling rate are adjusted so that the cast iron solidifies as a gray cast iron with spherical spheroidal graphite (GJS).
- GJS gray cast iron with spheroidal graphite
- the invention therefore also relates to a method for producing a drying cylinder in which a hollow roll body is cast from a cast iron, wherein the cast iron solidifies as gray cast iron with spheroidal graphite (GJS), and a hard material layer is applied to the outer peripheral surface of the roll body.
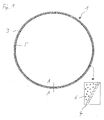
- a hollow roll body 1 of a drying cylinder for a tissue paper machine is shown in a cross section.
- the roller body 1 has a diameter of preferably at least 4 m and at most 6 m and a length of preferably at least 4 m and at most 7 m.
- the shell thickness of the roll body is preferably at least 40 mm and at most 100 mm.
- the roller body 1 is a cast body of gray cast iron (GJS) with freely embedded graphite, which is present at least substantially as spheroidal graphite.
- GJS gray cast iron
- the schematic detail view shown next to the cross section of the roller body 1 illustrates that the hollow roller body consists of gray-solidified cast iron with finely distributed graphite balls 6.
- a hard material layer 4 is applied, which has a thickness of preferably at least 0.1 mm and preferably at most 0.5 mm.
- the hard material layer 4 is advantageously applied by means of flame spraying or plasma spraying of ceramic material.
- the hard material layer 4 may comprise galvanically, electrolytically or autocatalytically deposited nickel or chromium or their compounds.
- the cavity of the roller body 1 can be subjected to a water vapor pressure of at least 2 bar, preferably at least 10 bar.
- the hollow roller body 1 thus forms a pressure vessel.
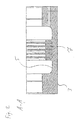
- circumferential ribs 7 are arranged on an inner surface 5 of the roller body 1 for improving the heat transfer and rigidity of the roller body 1.
- the circumferential ribs 7 are preferably machined in one piece from the material of the roller body 1.
- the circumferential ribs 7 are arranged at the same distance from each other.
- an inner cylinder can be arranged coaxially as a displacer within the roller body 1.
- the inner cylinder By means of the inner cylinder, the water vapor pressure to be acted upon volume of the roller body 1 can be reduced.
- a plurality of axially arranged spacer elements may be provided between the inner surface 5 of the roller body 1 and the outer surface of the inner cylinder. The Distance elements can advantageously improve both the heat transfer and the rigidity of the roll body 1.
Landscapes
- Paper (AREA)
- Rolls And Other Rotary Bodies (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL12150696T PL2474665T3 (pl) | 2011-01-11 | 2012-01-11 | Cylinder suszący do maszyny papierniczej tissue |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE202011001325U DE202011001325U1 (de) | 2011-01-11 | 2011-01-11 | Trockenzylinder für eine Tissue-Papiermaschine |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2474665A1 EP2474665A1 (de) | 2012-07-11 |
| EP2474665B1 true EP2474665B1 (de) | 2015-03-04 |
Family
ID=43735005
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12150696.8A Not-in-force EP2474665B1 (de) | 2011-01-11 | 2012-01-11 | Yankee-Zylinder für eine Tissue-Papiermaschine |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP2474665B1 (pl) |
| DE (1) | DE202011001325U1 (pl) |
| PL (1) | PL2474665T3 (pl) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11414718B2 (en) | 2017-06-01 | 2022-08-16 | Andritz Ag | Method for the surface treatment of a steel Yankee |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AT17293U1 (de) * | 2020-10-21 | 2021-11-15 | Valmet Oy | Yankee-trocknungszylinder und maschine zur herstellung von seidenpapier |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FI82094C (fi) * | 1989-02-16 | 1997-09-09 | Valmet Corp | Anvaendning av en legering av ett metallpulver och en karbid eller nitrid innefattande belaeggningskomposition foer en i en pappersmaskin anvaendbar yankeecylinder |
| US5171404A (en) * | 1990-11-30 | 1992-12-15 | S. D. Warren Company | Method and apparatus for calendering paper with internally heated roll |
| US6021581A (en) * | 1998-06-22 | 2000-02-08 | Voith Sulzer Paper Technology North America, Inc. | Method of drying a paper web in a paper-making machine at speeds greater than 6000 feet per minute |
| DE102004057480A1 (de) | 2004-11-19 | 2006-05-24 | Schäfer KG | Walze für die Herstellung von Bahnmaterial, vorzugsweise Tissue-Material |
| DE102009004562B4 (de) * | 2009-01-14 | 2015-06-03 | Shw Casting Technologies Gmbh | Walzenkörper für eine Walze zur Behandlung eines Materials und Verfahren zur Herstellung eines Walzenkörpers |
-
2011
- 2011-01-11 DE DE202011001325U patent/DE202011001325U1/de not_active Expired - Lifetime
-
2012
- 2012-01-11 PL PL12150696T patent/PL2474665T3/pl unknown
- 2012-01-11 EP EP12150696.8A patent/EP2474665B1/de not_active Not-in-force
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11414718B2 (en) | 2017-06-01 | 2022-08-16 | Andritz Ag | Method for the surface treatment of a steel Yankee |
Also Published As
| Publication number | Publication date |
|---|---|
| PL2474665T3 (pl) | 2015-11-30 |
| DE202011001325U1 (de) | 2011-03-10 |
| EP2474665A1 (de) | 2012-07-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2213790B1 (de) | Walzenkörper für eine Walze zur Behandlung eines Materials und Verfahren zur Herstellung eines Walzenkörpers | |
| DE69016161T2 (de) | Walze für die Papiererzeugung und Verfahren zu deren Herstellung. | |
| DE10164975B4 (de) | Bearbeitungskörper mit eingegossenem Hartstoffkörper | |
| DE69007828T2 (de) | Yankee-Zylinder und Verfahren zum Beschichten eines Yankee-Zylinders. | |
| EP2401532B1 (de) | Kolbenring | |
| DE69118455T2 (de) | Verschleissfester Gusseisenwerkstoff für eine Arbeitswalze und Verbundwalze | |
| EP2582456B1 (de) | Profilierte bandage für eine rollenpresse | |
| AT408666B (de) | Gusswerkstoff und verfahren zu dessen herstellung | |
| EP2401531B1 (de) | Kolbenringe | |
| EP1769098A1 (de) | Stahlband für streichmesser, auftragsmesser und kreppschaber und pulvermetallurgisches verfahren zu ihrer herstellung | |
| EP2474665A1 (de) | Trockenzylinder für eine Tissue-Papiermaschine | |
| DE69706608T2 (de) | Geschmiedete Rolle zum Walzen von nahtlosen Stahlrohren und Herstellungsverfahren | |
| DE69702974T2 (de) | Papiermasserefinerplatte aus einem rostfreier Stahllegierung | |
| EP0916407B2 (de) | Verfahren zur Herstellung einer Mahlwalze | |
| EP2386660B1 (de) | Gusskörper | |
| EP1804973B9 (de) | Presswalzen-ringbandage und verfahren zu ihrer herstellung | |
| EP3631023B1 (de) | Verfahren zur oberflächenbehandlung eines stahlyankees | |
| EP2354264B1 (de) | Verschleissbeständiger, warmfester Werkstoff, sowie dessen Verwendung | |
| EP3172352B1 (de) | Walze mit beschichtung | |
| DE202012007144U1 (de) | Profilierte Bandage für eine Rollenpresse | |
| AT408527B (de) | Metall-keramischer werkstoff und verfahren zu dessen herstellung | |
| DE10122886B4 (de) | Bearbeitungskörper mit eingegossenem Hartstoffkörper zum Zerkleinern eines Aufgabeguts | |
| DE102011002200B4 (de) | Verfahren zur Gewichtsreduzierung bzw. zur Steigerung der mechanischen Belastbarkeit von Bauteilen aus Gusseisenwerkstoffen | |
| WO2017001657A1 (de) | Bauteil für eine maschine zur herstellung und/oder behandlung einer faserstoffbahn und verfahren zur herstellung einer beschichtung eines bauteils | |
| EP1507023A1 (de) | Legierung zur Herstellung von verschleissresistenten Werkzeugen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| 17P | Request for examination filed |
Effective date: 20121127 |
|
| 17Q | First examination report despatched |
Effective date: 20131002 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20140804 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 714032 Country of ref document: AT Kind code of ref document: T Effective date: 20150415 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502012002376 Country of ref document: DE Effective date: 20150416 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20150304 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150604 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150605 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150706 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150704 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502012002376 Country of ref document: DE |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| 26N | No opposition filed |
Effective date: 20151207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20151223 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20160120 Year of fee payment: 5 Ref country code: IT Payment date: 20160127 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160131 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20160113 Year of fee payment: 5 Ref country code: SE Payment date: 20160120 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160111 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20160111 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20160930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160131 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160131 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160111 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160111 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502012002376 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170111 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170112 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170111 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 714032 Country of ref document: AT Kind code of ref document: T Effective date: 20170111 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170111 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20120111 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170111 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |