EP2176013B1 - Schmiededorn zum warmschmieden rohrförmiger werkstücke aus metall - Google Patents
Schmiededorn zum warmschmieden rohrförmiger werkstücke aus metall Download PDFInfo
- Publication number
- EP2176013B1 EP2176013B1 EP08773279A EP08773279A EP2176013B1 EP 2176013 B1 EP2176013 B1 EP 2176013B1 EP 08773279 A EP08773279 A EP 08773279A EP 08773279 A EP08773279 A EP 08773279A EP 2176013 B1 EP2176013 B1 EP 2176013B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- mandrel
- forging
- layer
- mandrel body
- hot
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Revoked
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21J—FORGING; HAMMERING; PRESSING METAL; RIVETING; FORGE FURNACES
- B21J13/00—Details of machines for forging, pressing, or hammering
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D9/00—Bending tubes using mandrels or the like
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21J—FORGING; HAMMERING; PRESSING METAL; RIVETING; FORGE FURNACES
- B21J13/00—Details of machines for forging, pressing, or hammering
- B21J13/08—Accessories for handling work or tools
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21K—MAKING FORGED OR PRESSED METAL PRODUCTS, e.g. HORSE-SHOES, RIVETS, BOLTS OR WHEELS
- B21K21/00—Making hollow articles not covered by a single preceding sub-group
Definitions
- the invention relates to a forging mandrel for hot forging tubular workpieces made of metal according to the preamble of claim 1.
- the hot forging of tubular workpieces is from the DE 10 2005 052 178 A1 known.
- a first forming step by punching a thick-walled hollow block is generated, which then by a radial forging process using a forged indenter inserted into the hollow block as an internal tool and at least two acting on the outer surface of the hollow block forging jaws of a forging machine forged to a seamless pipe.
- the hollow block is clocked rotated in the phase of the idle stroke of the forging jaws and moved axially.
- the forging mandrel is subjected to considerable thermal and mechanical stresses during the forging process, resulting in wear on the tool surface and reducing the life of the forging mandrel.
- the forging temperatures can be up to over 1300 ° C.
- This forge is subject to several disadvantages. On the one hand, this forging is very complex and expensive to manufacture, on the other hand, the heat input is not reduced in the mandrel material, which reduces the dimensional stability of the forging mandrel at high temperature stress and thus leads to premature failure.
- the object of the invention is to provide a forging mandrel for hot forging tubular workpieces made of metal, which is inexpensive to produce and has a high wear resistance at the same time great dimensional stability even at high forging temperatures.
- the mandrel material is made of a heat-resistant alloy, wherein the mandrel body is provided at least in the work area with a heat dissipation during forging in the mandrel body reducing and firmly adhering to the mandrel body layer and the layer has at least a thickness of 50 microns.
- the essential innovation of this invention is that the layer surrounding the mandrel body has a lower thermal conductivity than the mandrel body, whereby the heat input is significantly reduced in the mandrel body and thus a significantly improved dimensional stability is achieved even at high forging temperatures.
- the layer has a thermal conductivity which is significantly lower than that of the mandrel body material, advantageously at least 50%.
- the layer on the mandrel body can be produced according to the invention advantageously very inexpensively by scaling or by applying a corresponding layer z. B. by thermal processes.
- a scaling of the dome is advantageous to apply in carbon steels, while in highly alloyed Dorntechnikstoffen the layer advantageous by thermal spraying method, such. B. flame or plasma spraying can be applied.
- the thermally applied layers may contain, for example, zirconium oxide, aluminum oxide or iron oxide.
- this layer can exert a recognizable effect with regard to a significantly reduced heat input into the mandrel body, it is advantageous to carry out the layer with a minimum thickness of about 50 ⁇ m.
- the forging mandrel according to the invention has not only advantages in terms of improved dimensional stability even at high forging temperatures, but also with regard to a reduction of abrasive wear. Research has shown that there is some lubricity of the coating material during forging, which reduces abrasive wear.
- Essential for the selection of a suitable material for the mandrel body is to match this to the particular material to be forged so that welding of forging mandrel and forging workpiece is avoided.
- the forging mandrel according to the invention has the advantageous effect that the layer acts on the mandrel body as a release layer, which counteracts welding under forging pressure and temperature.
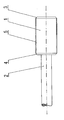
- the forging mandrel shown in the single figure has a provided with chamfers 3, 4 mandrel body 1 which is fixed to a support rod 2.
- the support rod 2 is required to axially and rotatably move the forging mandrel in a tubular workpiece, not shown here.
- the mandrel body 1 consists of a heat-resistant steel which according to the invention is provided with a layer 5 which reduces the heat input into the mandrel body 1 in the working area.
- the layer 5 in this case has a significantly lower thermal conductivity than the material of the mandrel body 1 in order to reduce the heat input and thus to ensure the dimensional stability of the mandrel body 1, even at high forging temperatures.
- the mandrel body 1 is formed in the present case as a solid body, but it is also possible to provide this with an internal cooling to dissipate the unavoidable heat input into the mandrel body 1 during the forging as quickly as possible.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Forging (AREA)
- Coating By Spraying Or Casting (AREA)
Description
- Die Erfindung betrifft einen Schmiededorn zum Warmschmieden rohrförmiger Werkstücke aus Metall gemäß dem Oberbegriff des Patentanspruches 1.
- Das Warmschmieden rohrförmiger Werkstücke, wie z.B. nahtloser Stahlrohre, ist aus der
DE 10 2005 052 178 A1 bekannt. - Bei diesem Verfahren wird ausgehend von einem auf Umformtemperatur erwärmten Block, in einem ersten Umformschritt durch Lochen ein dickwandiger Hohlblock erzeugt, der anschließend durch einen Radialschmiedeprozess unter Verwendung eines in den Hohlblock eingeschobenen Schmiededorns als Innenwerkzeug und mindestens zwei auf die Mantelfläche des Hohlblockes einwirkender Schmiedebacken einer Schmiedemaschine zu einem nahtlosen Rohr geschmiedet wird. Dabei wird der Hohlblock getaktet in der Phase des Leerhubes der Schmiedebacken gedreht und axial verschoben.
- Der Schmiededorn wird während des Schmiedeprozesses beträchtlichen thermischen und mechanischen Beanspruchungen ausgesetzt, was zu Verschleißerscheinungen an der Werkzeugoberfläche führt und die Standzeit des Schmiededorns herabsetzt. Beispielsweise können die Schmiedetemperaturen bis über 1300°C betragen.
- Um thermisch bedingte Verschleißerscheinungen zu minimieren ist es aus der gattungsgemäßen
DE 2825940 A1 bekannt, den Schmiededorn von der Innenseite her zu kühlen, um die Wärmeabfuhr von der Oberfläche des Dorns in den Dorn hinein zu beschleunigen. - Um die Verschleißfestigkeit des Dorns zu erhöhen, wird weiterhin vorgeschlagen, den Dornkörper mit einem Außenmantel aus hochwarmfesten Werkstoff wie z.B. einer Nickel- oder Kobaltbasislegierung zu umgeben.
- Dieser Schmiededorn ist mit mehreren Nachteilen behaftet. Zum einen ist dieser Schmiededorn sehr aufwändig und teuer in der Herstellung, zum anderen wird der Wärmeeintrag in den Dornwerkstoff nicht verringert, was bei hoher Temperaturbeanspruchung die Formstabilität des Schmiededorns verringert und damit zu einem frühzeitigen Ausfall führt.
- Aufgabe der Erfindung ist es, einen Schmiededorn zum Warmschmieden rohrförmiger Werkstücke aus Metall anzugeben, der kostengünstig herstellbar ist und eine hohe Verschleißfestigkeit bei gleichzeitig großer Formstabilität auch bei hohen Schmiedetemperaturen aufweist.
- Diese Aufgabe wird ausgehend vom Oberbegriff in Verbindung mit dem kennzeichnenden Teil des Anspruches 1 gelöst. Vorteilhafte Weiterführungen sind Gegenstand von Unteransprüchen.
- Nach der Lehre der Erfindung besteht der Dornwerkstoff aus einer warmfesten Legierung, wobei der Dornkörper mindestens im Arbeitsbereich mit einer die Wärmeableitung während des Schmiedens in den Dornkörper vermindernden und auf dem Dornkörper fest haftenden Schicht versehen ist und die Schicht mindestens eine Dicke von 50 µm aufweist.
- Die wesentliche Neuerung dieser Erfindung ist, dass die den Dornkörper umgebende Schicht eine geringere Wärmeleitfähigkeit als der Dornkörper aufweist, wodurch der Wärmeeintrag in den Dornkörper deutlich vermindert und damit eine deutlich verbesserte Formstabilität auch bei hohen Schmiedetemperaturen erreicht wird.
- Die Schicht weist dabei erfindungsgemäß eine Wärmeleitfähigkeit auf, die deutlich unter derjenigen des Dornkörperwerkstoffes liegt, vorteilhaft um mindestens 50 %.
- Die Schicht auf dem Dornkörper kann dabei erfindungsgemäß vorteilhaft sehr kostengünstig durch Verzundern erzeugt werden oder aber durch Auftragen einer entsprechenden Schicht z. B. durch thermische Verfahren.
- Eine Verzunderung des Domes ist dabei vorteilhaft bei Kohlenstoffstählen anzuwenden, während bei hochlegierten Dornwerkstoffen die Schicht vorteilhaft durch thermische Spritzverfahren, wie z. B. Flamm- oder Plasmaspritzen aufgebracht werden kann.
- Die thermisch aufgebrachten Schichten können dabei beispielsweise Zirkoniumoxid, Aluminiumoxid oder Eisenoxid enthalten.
- Wesentlich ist dabei, dass die Wärmeleitfähigkeit des Beschichtungsmaterials immer deutlich unter derjenigen des Dornwerkstoffs liegt.
- Damit diese Schicht eine erkennbare Wirkung im Hinblick auf einen deutlich verminderten Wärmeeintrag in den Dornkörper ausüben kann, ist es vorteilhaft die Schicht mit einer Mindestdicke von ca. 50 µm auszuführen.
- Der erfindungsgemäße Schmiededorn weist dabei nicht nur Vorteile im Hinblick auf eine verbesserte Formstabilität auch bei hohen Schmiedetemperaturen auf, sondern auch im Hinblick auf eine Verringerung des abrasiven Verschleißes. In Untersuchungen hat sich herausgestellt, dass eine gewisse Schmierwirkung des Schichtmaterials beim Schmieden vorhanden ist, die den abrasiven Verschleiß reduziert.
- Wesentlich für die Auswahl eines geeigneten Werkstoffes für den Dornkörper ist, diesen auf den jeweils zu schmiedenden Werkstoff so abzustimmen, dass ein Verschweißen von Schmiededorn und Schmiedewerkstück vermieden wird.
- Der erfindungsgemäße Schmiededorn weist dabei den vorteilhaften Effekt auf, dass die Schicht auf dem Dornkörper als Trennschicht wirkt, die einem Verschweißen unter Schmiededruck und Temperatur entgegenwirkt.
- Da ein gewisser Wärmeeintrag in den Dornkörper nicht vollständig unterbunden werden kann, kann es zur Unterstützung der Formstabilität des Dorns darüber hinaus sinnvoll sein, den Dornkörper mit einer zusätzlichen Innenkühlung zu versehen.
- Alternativ kann aber auch vorgesehen werden, in Stillstandsphasen den Dornkörper von außen zu kühlen, was sehr viel kostengünstiger zu realisieren ist, als eine Innenkühlung.
- Um den Wärmeeintrag in den Dornkörper während des Schmiedevorgangs auf ein Minimum zu beschränken, kann es darüber hinaus sinnvoll sein, den Dorn beim Schmieden im Werkstück zu verfahren, da bei diesem Vorgang immer andere Arbeitsbereiche der Schmiededornoberfläche in Eingriff gelangen und so der lokale Wärmeeintrag reduziert wird.
- Der erfindungsgemäße Schmiededorn wird anhand einer Darstellung näher beschrieben.
- Der in der einzigen Figur dargestellte Schmiededorn, weist einen mit Fasen 3, 4 versehenen Dornkörper 1 auf, der an einer Haltestange 2 befestigt ist. Die Haltestange 2 wird benötigt, um den Schmiededorn in einem hier nicht dargestellten rohrförmigen Werkstück axial und drehbar verfahren zu können.
- Der Dornkörper 1 besteht aus einem warmfesten Stahl, der erfindungsgemäß mit einer im Arbeitsbereich die Wärmeeinleitung in den Dornkörper 1 vermindernden Schicht 5 versehen ist.
- Die Schicht 5 weist dabei eine deutlich niedrigere Wärmeleitfähigkeit auf, als der Werkstoff des Dornkörpers 1, um den Wärmeeintrag zu reduzieren und damit die Formstabilität des Dornkörpers 1 auch bei hohen Schmiedetemperaturen zu gewährleisten.
- Der Dornkörper 1 ist im vorliegenden Fall als Massivkörper ausgebildet, es ist jedoch auch möglich, diesen mit einer Innenkühlung zu versehen, um den unvermeidbaren Wärmeeintrag in den Dornkörper 1 während des Schmiedens möglichst rasch abzuführen.
-
Nr. Bezeichnung 1 Dornkörper 2 Haltestange 3,4 Fase 5 Schicht
Claims (6)
- Schmiededorn zum Warmschmieden rohrförmiger Werkstücke aus Metall, bestehend aus einem Dornkörper und einer Dornstange, bei dem der Dornkörper aus einem warmfesten Werkstoff besteht
dadurch gekennzeichnet,
dass der Dornkörper (1) mindestens im Arbeitsbereich mit einer die Wärmeableitung während des Schmiedens in den Dornkörper vermindernden und auf dem Dornkörper (1) fest haftenden Schicht (5) versehen ist, wobei die Schicht (5) eine geringere Wärmeleitfähigkeit als der Werkstoff des Dornkörpers (1) und mindestens eine Dicke von 50 µm aufweist. - Schmiededorn nach Anspruch 1
dadurch gekennzeichnet,
dass die Schicht (5) eine Zunderschicht ist. - Schmiededorn nach Anspruch 1
dadurch gekennzeichnet,
dass die Schicht (5) flammgespritzt ist. - Schmiededorn nach Anspruch 1
dadurch gekennzeichnet,
dass die Schicht (5) plasmagespritzt ist. - Schmiededorn nach einem der vorstehenden Ansprüche
dadurch gekennzeichnet,
dass die Wärmeleitfähigkeit der Schicht (5) mindestens 50 % geringer ist, als die Wärmeleitfähigkeit des Dornwerkstoffs. - Schmiededorn nach einem der Ansprüche 1 - 5
dadurch gekennzeichnet,
dass der Dornkörper (1) als mit einer einseitigen Öffnung versehener Hohlkörper ausgebildet und mit einer mindestens bis in den Arbeitsbereich sich erstreckenden Innenkühleinrichtung versehen ist.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL08773279T PL2176013T3 (pl) | 2007-07-10 | 2008-06-25 | Przebijak kowalski do kucia na gorąco mających kształt rury przedmiotów obrabianych z metalu |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102007032804A DE102007032804B3 (de) | 2007-07-10 | 2007-07-10 | Schmiededorn zum Warmschmieden rohrförmiger Werkstücke aus Metall |
| PCT/DE2008/001067 WO2009006873A1 (de) | 2007-07-10 | 2008-06-25 | Schmiededorn zum warmschmieden rohrförmiger werkstücke aus metall |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2176013A1 EP2176013A1 (de) | 2010-04-21 |
| EP2176013B1 true EP2176013B1 (de) | 2010-10-27 |
Family
ID=39670381
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08773279A Revoked EP2176013B1 (de) | 2007-07-10 | 2008-06-25 | Schmiededorn zum warmschmieden rohrförmiger werkstücke aus metall |
Country Status (17)
| Country | Link |
|---|---|
| US (1) | US20100251794A1 (de) |
| EP (1) | EP2176013B1 (de) |
| JP (1) | JP2010532715A (de) |
| KR (1) | KR20100030628A (de) |
| CN (1) | CN101743077B (de) |
| AR (1) | AR067462A1 (de) |
| AT (1) | ATE485903T1 (de) |
| AU (1) | AU2008274744B2 (de) |
| BR (1) | BRPI0812826A2 (de) |
| CA (1) | CA2693450A1 (de) |
| DE (2) | DE102007032804B3 (de) |
| EA (1) | EA015221B1 (de) |
| ES (1) | ES2355125T3 (de) |
| PL (1) | PL2176013T3 (de) |
| UA (1) | UA96053C2 (de) |
| WO (1) | WO2009006873A1 (de) |
| ZA (1) | ZA200908608B (de) |
Families Citing this family (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2241386A1 (de) * | 2009-04-16 | 2010-10-20 | Felss GmbH | Umformwerkzeug zur Herstellung eines Innenprofils, insbesondere einer Innenverzahnung, eines Werkstücks |
| DE102009053166B4 (de) | 2009-11-02 | 2015-02-19 | V & M Deutschland Gmbh | Verfahren und Einrichtung zum optimierten Stangenumlauf bei der Herstellung eines nahtlos warmgefertigten Stahlrohres nach dem Rohrkontiverfahren |
| AT511745B1 (de) * | 2011-08-12 | 2014-09-15 | Gfm Gmbh | Vorrichtung zum schmieden eines hohlkörpers |
| AT511748B1 (de) * | 2011-08-12 | 2014-04-15 | Gfm Gmbh | Vorrichtung zum schmieden eines hohlkörpers |
| DE102013219310A1 (de) | 2013-09-25 | 2015-03-26 | Gfm Gmbh | Verfahren zum Warmschmieden eines nahtlosen Hohlkörpers aus schwer umformbarem Werkstoff, insbesondere aus Stahl |
| CN104275363A (zh) * | 2013-11-30 | 2015-01-14 | 阜新华通管道有限公司 | 高温高压管件用无缝钢管随形胎锻造方法 |
| JP6521369B2 (ja) * | 2015-05-11 | 2019-05-29 | 日立金属株式会社 | 熱間鍛造用金型 |
| US11122741B2 (en) * | 2018-01-30 | 2021-09-21 | Cnh Industrial America Llc | Stalk roller assembly for an agricultural system |
| CN117920927B (zh) * | 2024-01-31 | 2026-05-08 | 西安稀有金属材料研究院有限公司 | 一种锆合金燃料组件导向管的高精度制备装置和方法 |
Family Cites Families (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AT350356B (de) * | 1977-08-30 | 1979-05-25 | Gfm Fertigungstechnik | Schmiededorn |
| JPS5913924B2 (ja) * | 1979-12-25 | 1984-04-02 | 日本鋼管株式会社 | 穿孔圧延機用芯金 |
| JPS61110770A (ja) * | 1984-11-01 | 1986-05-29 | Sumitomo Electric Ind Ltd | 熱間加工用超硬合金工具 |
| JPH01135143U (de) * | 1988-03-09 | 1989-09-14 | ||
| CA2025302A1 (en) * | 1989-12-26 | 1991-06-27 | General Electric Company | Reinforced microlaminted metal-matrix-composite structure |
| JP3191008B2 (ja) * | 1991-04-04 | 2001-07-23 | 日立金属株式会社 | 熱間工具鋼 |
| JP3124442B2 (ja) * | 1994-06-21 | 2001-01-15 | 新日本製鐵株式会社 | 傾斜機能を有する鍛造用工具及びその製造方法 |
| CN2458107Y (zh) * | 2000-12-27 | 2001-11-07 | 中国科学院广州能源研究所 | 一种锻模的电辐射预热装置 |
| DE10124866A1 (de) * | 2001-05-22 | 2002-12-05 | Peter Schuele | Werkzeug für Biegemaschine |
| JP2004066246A (ja) * | 2002-08-01 | 2004-03-04 | Osg Corp | 球面バニッシュ転造丸ダイス、及び、その製造方法 |
| JP2004255429A (ja) * | 2003-02-26 | 2004-09-16 | Honda Motor Co Ltd | 高ヤング率高疲労強度鋼の加工方法 |
| CN2657903Y (zh) * | 2003-12-11 | 2004-11-24 | 株洲时代新材料科技股份有限公司 | 中大型橡胶模具加热器 |
| EP1728566B1 (de) * | 2004-03-11 | 2012-08-29 | Sumitomo Metal Industries, Ltd. | Vorrichtung zur herstellung nahtloser rohre und diese verwendendes verfahren zur herstellung nahtloser rohre |
| DE102005052178B4 (de) * | 2004-10-25 | 2008-06-19 | V&M Deutschland Gmbh | Verfahren zum Herstellen eines nahtlos warmgefertigten Stahlrohres |
| CN100358652C (zh) * | 2005-12-06 | 2008-01-02 | 武汉理工大学 | 一种热锻模及其制备方法 |
| US7587923B1 (en) * | 2006-07-12 | 2009-09-15 | Raul Garza | Method of making a tubular |
| JP4910693B2 (ja) * | 2006-12-28 | 2012-04-04 | 住友金属工業株式会社 | マンドレルバーへの潤滑剤の塗布方法、マンドレルバーへの潤滑剤の膜厚管理方法および継目無鋼管の製造方法。 |
| JP5169982B2 (ja) * | 2009-03-03 | 2013-03-27 | 新日鐵住金株式会社 | プラグ、穿孔圧延機、およびそれを用いた継目無管の製造方法 |
-
2007
- 2007-07-10 DE DE102007032804A patent/DE102007032804B3/de not_active Expired - Fee Related
-
2008
- 2008-06-25 KR KR1020097027175A patent/KR20100030628A/ko not_active Ceased
- 2008-06-25 JP JP2010515345A patent/JP2010532715A/ja not_active Withdrawn
- 2008-06-25 US US12/668,282 patent/US20100251794A1/en not_active Abandoned
- 2008-06-25 AT AT08773279T patent/ATE485903T1/de active
- 2008-06-25 AU AU2008274744A patent/AU2008274744B2/en not_active Ceased
- 2008-06-25 BR BRPI0812826-0A2A patent/BRPI0812826A2/pt not_active IP Right Cessation
- 2008-06-25 ES ES08773279T patent/ES2355125T3/es active Active
- 2008-06-25 WO PCT/DE2008/001067 patent/WO2009006873A1/de not_active Ceased
- 2008-06-25 DE DE502008001670T patent/DE502008001670D1/de active Active
- 2008-06-25 EP EP08773279A patent/EP2176013B1/de not_active Revoked
- 2008-06-25 CA CA2693450A patent/CA2693450A1/en not_active Abandoned
- 2008-06-25 UA UAA201001359A patent/UA96053C2/ru unknown
- 2008-06-25 EA EA201000187A patent/EA015221B1/ru not_active IP Right Cessation
- 2008-06-25 CN CN200880023941XA patent/CN101743077B/zh not_active Expired - Fee Related
- 2008-06-25 PL PL08773279T patent/PL2176013T3/pl unknown
- 2008-07-07 AR ARP080102919A patent/AR067462A1/es active IP Right Grant
-
2009
- 2009-12-03 ZA ZA2009/08608A patent/ZA200908608B/en unknown
Also Published As
| Publication number | Publication date |
|---|---|
| CN101743077B (zh) | 2011-07-13 |
| DE502008001670D1 (de) | 2010-12-09 |
| KR20100030628A (ko) | 2010-03-18 |
| EA201000187A1 (ru) | 2010-06-30 |
| DE102007032804B3 (de) | 2008-09-04 |
| EA015221B1 (ru) | 2011-06-30 |
| WO2009006873A9 (de) | 2010-01-21 |
| BRPI0812826A2 (pt) | 2014-12-09 |
| WO2009006873A1 (de) | 2009-01-15 |
| AU2008274744A1 (en) | 2009-01-15 |
| ATE485903T1 (de) | 2010-11-15 |
| AR067462A1 (es) | 2009-10-14 |
| AU2008274744A2 (en) | 2010-04-15 |
| AU2008274744B2 (en) | 2011-07-14 |
| ES2355125T3 (es) | 2011-03-23 |
| CA2693450A1 (en) | 2009-01-15 |
| UA96053C2 (ru) | 2011-09-26 |
| PL2176013T3 (pl) | 2011-05-31 |
| JP2010532715A (ja) | 2010-10-14 |
| ZA200908608B (en) | 2011-02-23 |
| US20100251794A1 (en) | 2010-10-07 |
| EP2176013A1 (de) | 2010-04-21 |
| CN101743077A (zh) | 2010-06-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE102007032804B3 (de) | Schmiededorn zum Warmschmieden rohrförmiger Werkstücke aus Metall | |
| EP2851138B1 (de) | Partiell gekühltes Warmformwerkzeug | |
| EP2544838B1 (de) | Verfahren zum herstellen eines kühlbaren formwerkzeugs sowie durch das verfahren hergestelltes formwerkzeug | |
| EP1888794B1 (de) | Verfahren zum herstellen eines metallbauteils mit aneinander angrenzenden abschnitten unterschiedlicher materialeigenschaften | |
| EP2548670B1 (de) | Umformwerkzeug und Verfahren zur Herstellung von Formbauteilen aus Metallplatinen | |
| EP3160667B1 (de) | Verfahren und umformwerkzeug zum warmumformen sowie entsprechendes werkstück | |
| EP2059355A1 (de) | Verfahren und werkzeug zum warmumformen eines metallwerkstücks | |
| WO2014019723A1 (de) | Zylinderlaufbuchse und verfahren zu deren herstellung | |
| EP3088084B1 (de) | Hartkörper als rasterpanzerung für eine rollenpresse, verfahren zu dessen herstellung, und rolle für eine rollenpresse | |
| DE19630115A1 (de) | Verfahren zum Herstellen eines Kegelrades | |
| DE102004018921A1 (de) | Verfahren zur Herstellung einer Pleuelstange sowie eines Kolbenbolzens | |
| EP2542361B1 (de) | Verfahren zur herstellung eines warmwerkzeugs mit einer beschichtung | |
| DE102009025621B4 (de) | Verfahren zum Herstellen eines metallischen Bauteils mit einer gehärteten Oberflächenschicht sowie danach hergestelltes Bauteil | |
| EP2554293A1 (de) | Rohrschmiedeverfahren mit urgeformtem Hohlblock | |
| EP2864063B1 (de) | Verfahren zur herstellung einer verbundwalze und damit hergestellte verbundwalze | |
| DE102012010916A1 (de) | Schweißwerkzeug und Verfahren zur Herstellung desselben | |
| DE102018001712A1 (de) | Vorrichtung und Verfahren zum Reibdrücken zur Erzeugung von umgeformten Bereichen, insbesondere von Flanschstrukturen, an profilförmigen Werkstücken | |
| DE10311150A1 (de) | Verfahren zur Herstellung eines geschmiedeten Kolbens für einen Verbrennungsmotor | |
| CN105583585A (zh) | 一种低碳合金钢制动鼓的加工工艺 | |
| DE10022884B4 (de) | Verfahren zur Bruchtrennung in Bauteilen oder deren Vormaterial | |
| DE102015217525A1 (de) | Nietverbindung und Verfahren zum Herstellen einer Nietverbindung | |
| DE102016117914A1 (de) | Verfahren zum Herstellen eines Bauteils oder Halbzeugs sowie Vorrichtung zur Durchführung desselben | |
| DE102013010919B4 (de) | Verfahren zur Bearbeitung eines Werkstückes sowie ein mit diesem Verfahren hergestelltes Formteil | |
| EP4417336B1 (de) | Verfahren zum härten und richten hochlegierter werkzeugstähle | |
| EP1344584B1 (de) | Umformwerkzeug und Verfahren zum spanlosen Umformen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20091211 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA MK RS |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| DAX | Request for extension of the european patent (deleted) | ||
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 502008001670 Country of ref document: DE Date of ref document: 20101209 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20101027 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2355125 Country of ref document: ES Kind code of ref document: T3 Effective date: 20110323 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20101027 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110127 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110227 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110228 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110127 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110128 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: DURUM, VERSCHLEISS-SCHUTZ GMBH Effective date: 20110720 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R026 Ref document number: 502008001670 Country of ref document: DE Effective date: 20110720 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 |
|
| BERE | Be: lapsed |
Owner name: V & M DEUTSCHLAND G.M.B.H. Effective date: 20110630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110630 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502008001670 Country of ref document: DE Effective date: 20120103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120103 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20120627 Year of fee payment: 5 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20120625 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120630 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110630 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120625 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110625 Ref country code: CY Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20101027 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20130618 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20130703 Year of fee payment: 6 Ref country code: IT Payment date: 20130626 Year of fee payment: 6 Ref country code: PL Payment date: 20130524 Year of fee payment: 6 Ref country code: RO Payment date: 20130603 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101027 |
|
| RDAF | Communication despatched that patent is revoked |
Free format text: ORIGINAL CODE: EPIDOSNREV1 |
|
| RDAG | Patent revoked |
Free format text: ORIGINAL CODE: 0009271 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT REVOKED |
|
| 27W | Patent revoked |
Effective date: 20131023 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MA03 Ref document number: 485903 Country of ref document: AT Kind code of ref document: T Effective date: 20131023 |