EP1900864B1 - Process and device for continuously mercerising spun yarn - Google Patents
Process and device for continuously mercerising spun yarn Download PDFInfo
- Publication number
- EP1900864B1 EP1900864B1 EP20070115878 EP07115878A EP1900864B1 EP 1900864 B1 EP1900864 B1 EP 1900864B1 EP 20070115878 EP20070115878 EP 20070115878 EP 07115878 A EP07115878 A EP 07115878A EP 1900864 B1 EP1900864 B1 EP 1900864B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- threads
- yarn
- mercerising
- strip
- alkaline solution
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images



Classifications
-
- D—TEXTILES; PAPER
- D06—TREATMENT OF TEXTILES OR THE LIKE; LAUNDERING; FLEXIBLE MATERIALS NOT OTHERWISE PROVIDED FOR
- D06B—TREATING TEXTILE MATERIALS USING LIQUIDS, GASES OR VAPOURS
- D06B7/00—Mercerising, e.g. lustring by mercerising
- D06B7/04—Mercerising, e.g. lustring by mercerising of yarns, threads or filaments
-
- D—TEXTILES; PAPER
- D10—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B2201/00—Cellulose-based fibres, e.g. vegetable fibres
Definitions
- the present invention refers to the mercerising treatment of cotton yarn to give them the desired characteristics for their end use to produce fabrics or other manufactured products.
- the treatment of yarn with liquid reactants uses a large variety of processes, for the various types of fibres like cotton, wool, silk, linen and so on, with which the yarn is given the desired characteristics or undesired components that decrease its worth and its possibilities of use are removed from it.
- such treatment is typically mercerisation, but it can also concern other treatments like dyeing, bleaching and so on.
- the mercerising treatment of cotton yarn improves its mechanical characteristics, improves it appearance, and enhances its absorption capacity and reactivity towards finishing products and the affinity towards dyes.
- it consists of treating yarn with highly concentrated alkaline solutions followed by drawing and removal of the reactants with suitable washes.
- the treatment is carried out on individual fibres that make up the yarn in a semi-plastic state induced by the concentrated alkalis that imbibe them.
- the mercerisation is typically carried out on the yarn in skeins, prepared with a reeling stage, subjected to discontinuous mercerisation, and then washed, neutralised, dried, unwound and repacked in reels.
- DE 41 21 593 discloses an impregnating device for treating thread, in which the thread circulates several times around one couple of vertical parallel rotating rolls having their bottom immersed into the treating medium.
- GB 960.150 discloses a device for applying the size on a warp, consisting of a jet tube spraying the size on the individual threads of the warp kept in tension within a damming chamber.
- the purpose of the present invention is to make a system for continuously treating yarn with process fluids, and specifically mercerisation, which allows the drawbacks of the systems used or proposed in the state of the art to be overcome.
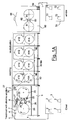
- FIGS 1A-B illustrate the general scheme of the system for continuously treating yarn with process fluids.
- Figure 2 and the detail of figure 2A illustrate the relevant details of the first device for imbibing the threads subjected to mercerisation.
- Figure 3 illustrates the essential details of the container in which the mercerisation reaction takes place.
- Figure 4 illustrates the details of the hydro-extraction and drawing device after the mercerising reaction.
- Figure 5 then illustrates the details of the container 40 in which the drawing of the yarn and its first washing with water take place.
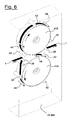
- Figure 6 illustrates the containers 40bis in which both the second washing and the neutralisation stages take place.
- figure 7 illustrates the details of the container 60 in which the drying and dehydration stage of the mercerised threads takes place.
- the yarn 1 to be treated is fed from a series of reels 2 arranged in parallel on a creel 3.
- the reels 2 yield a plurality of threads 1, which are kept separate and parallel during the entire process and along the entire sequence of mercerising apparatuses.
- the processing must be carried out on a congruous number of parallel threads 1, at least of the order of a few tens of threads at once, unwound with a speed at least of the order of 5-10 m/sec.
- the return of the parallel threads 1 is carried out with the pair of main guide rollers 4 with horizontal axis, which rotate at controlled speed and that determine the linear flow rate of the threads being processed taken to the mercerising unit, operating as outlined above at a linear speed of at least 5-10 m/sec.
- a relevant characteristic of the present invention lies in the operation of the treatment and in the structure of the mercerising reactor in which the treatment of the threads is carried out with sodium hydroxide alkaline solution.
- Such an operation is carried out in a closed parallelepiped-shaped container 5.
- the closed container 5 in general shaped like a wardrobe that can be opened for the intervention of operators, it is possible to maintain a controlled atmosphere, just like for the other further containers foreseen in the unit.
- the group of parallel threads 1 is deviated and guided firstly with rollers 7 with horizontal axis and worked with radial grooves that allow the threads to be kept separate and spaced apart during the entire mercerising reaction.
- the strip of parallel and separated threads 1 is fed to a first imbibing device 8 illustrated in greater detail in figure 2 , which shows plan, front and side section views. It consists of an imbibing plate 10 equipped with longitudinal grooves 11 that are independent and have constant pitch, which guide the threads 1 separately.
- the mercerising fluid consists of the alkaline solution, for example sodium hydroxide at 30° Be, and is sprayed on the plate 10 with sprayers 12 with nozzles at the grooves 11 in which the threads 1 run at a speed controlled by the initial guide rollers 4.
- the top part of the grooved plate 10 is protected with a cover 13.
- a sealing device 15 is arranged at the entry of the strip of threads 1 into the imbibing device 8 . It consists of an elongated tank 16, fed with the same mercerising solution and kept at atmospheric pressure, with a lower slit that comes out onto the grooves that guide and contain the threads in movement from left to right in the drawing according to the arrows F.
- the liquid head of the tank 16 allows a first imbibition at atmospheric pressure of the threads 1 and avoids the entry of air into the second treatment area with the pressurised solution.
- the plate 10 is worked with V-shaped grooves, whereas the cover 13 is provided with one or more sprayers 12 consisting of a series of pressurised injection micro-nozzles 18, shown in the detail of figure 2A and each arranged at each individual groove 11 crossed by a single thread.
- Each sprayer 12 and the tank 16 are fed with fittings 17 from a general feeding duct, not shown in the figures, which takes the alkaline mercerising solution at constant pressure and at controlled temperature.
- the temperature of the mercerising solution is kept at 30-35°C, whereas the injection overpressure is between 1 and 15 bars, preferably between 1.5 and 4 bars. Indeed, it has been found that the injection overpressure of the mercerising fluid causes a substantial increase in the mercerisation reaction kinetics, which can be attributed to a better exchange coefficient and a more efficient contact between the liquid phase and cellulose micelles, substantially accelerating the mercerising reaction. In conventional mercerisation techniques by immersion in baths or recipients at atmospheric pressure contact times of the order of minutes are required, whereas the technical solution according to the present invention allows such contact times to be drastically reduced, reducing them to the order of magnitude of 10 seconds.
- the structure and the operation of the rotary drums 20 and of the other elements inside the container 5 is illustrated in greater detail in figure 3 , in which they are shown in perspective view and transparently.
- the drums 20 are mounted parallel with substantially horizontal axis and they are equipped with a substantially smooth cylindrical surface.
- the incomplete 8-shaped spirals 21 are deposited on the surface of the drums 20.
- the deposit of the strip of threads 1 is guided with rotary combs 22, made up of a series of grooved ceramic bushings mounted with constant pitch on a shaft, and with the deviating rollers 24.
- the deviating rollers 24 have a substantially smooth surface, they are mounted with oblique rotation axis with respect to the axes of the drums 20 and they are equipped with means for varying their inclination.
- the inclination to the right or left of the axes of the deviating rollers 24 allows the progressive axial gauge between the 8-shaped spirals that wind on the drums 20 to be determined.
- the whole of the threads 1 in a strip enters into the rear part at the main guide rollers 4, passes the imbibing device 8, winds - starting from the right-hand drum 20 - with 8-shaped spirals that advance towards the front part of the container 5, and discharges - from the left-hand drum 20 - through the hydro-extraction and drawing device 27.
- imbibing device 8 to the hydro-extraction device 27 the mercerising reaction between the cellulose micelles of the yarn and the solution that imbibes the yarn itself takes place.
- the variation in inclination of the axes of the deviating rollers 24 allows the progressive axial gauge to be generated between the 8-shaped spirals that wind on the drums 20 and allows the number of spirals that can be carried by the available length of the drums 20 to be varied, thus determining the length of the path of the strip of threads 1 and its treatment time with alkaline solution.
- substantially "square" cylindrical drums 20 with a diameter and length of about 1000 mm, it is possible to wind 50-100 m of strip of threads 1 and to carry out reaction times within the range of 8-15 seconds, which corresponds to the time of complete "re-entry", in other words the time for completion of the reactions between the cellulose and the alkaline solution, which result in the shortening of the yarn by values of 10-20% according to the type of yarn and the original cotton.
- one or more series of further spray nozzles is arranged close to the surface of the drums themselves, to renew the contact between yarn and alkaline solution.
- Such spray nozzles are placed on nozzle-carrying rods 25 and are analogous to those that equip the imbibing device 8, but operating at lower pressure, and the position of a pair of rods 25 thereof is shown as an example in figure 1A .
- the strip of threads 1 is discharged with the hydro-extraction and drawing device 27 after the mercerising reaction. It is shown in figure 4 with its essential components.
- the strip of mercerised threads 1 still imbibed with alkaline solution passes from idle deviating rollers 28 and reaches the hydro-extraction device 29 consisting of a motorised roller 30 against which two idle counter-rollers 31 are pressed, preferably made from polymeric elastic material.
- Such a roller 30 rotates at the linear speed of the strip of threads 1 fed, decreased by the expected percentage shrinkage for the mercerisation.
- All of the motorisations of the shafts of the rotary members inside the container 5, in other words the drums 20, the rotary combs 22, the deviating rollers 24 and the roller 30, are controlled with independent actuations, for example through inverters, and the various angular speeds are synchronised with each other to obtain and keep the linear speeds for the drums 20 and the deviating rollers 24 coherent with that of the strip of threads 1 being processed.
- the rotation speed of the combs 22, on the other hand, is lower (2-10 revolutions per minute); it is carried out to limit the erosion phenomena of the ceramic bushes of which they consist.
- a device 35 for capturing the ends of the threads that have broken is arranged at the motorised roller 30 of the hydro-extraction device 29. Indeed, there is greater probability of breaking at the drawing of the mercerised threads and, in this case, the ends tend to stick and wind onto the roller 30.
- the device 35 for example, can consist of a suction mouth 36 connected to a suction duct 37; the top edge of its suction slit 38 is made from polymeric material and is arranged to scrape the metallic surface of the roller 30. In this way, the possible end that winds onto the surface of said roller is stopped and sucked up by the mouth 36.
- the device 35 for capturing the ends can be made with a rotary brush of bristles made from polymeric material that, mounted in the same position as the mouth 36 and made to rotate at a high speed, clears the roller 30 of the possible ends that would otherwise wind onto its surface.
- said strip After passing into the container 5 in which the contact is made between the threads 1 in a strip and the alkaline mercerising solution, said strip is fed for washing with water.
- the washing can be carried out in many stages with water in countercurrent and at decreasing temperature, according to methods already known in the field.
- the first washing stage is carried out in the container 40, illustrated in figure 5 with its essential components. In it the washing operation of the yarn treated with the alkaline solution and coming from the container 5 takes place.
- the strip of threads 1 is guided and deviated by a series of idle rollers 28 up to the rotary cylindrical drums 41A, B made from metallic material and with a smooth surface.
- the strip of threads is inserted and held between the surface of the drums 41A, B and a series of idle cylindrical counter-rollers 42 that wrap around them and are kept pressed to grip said strip. At each passage under such counter-rollers the liquid contained by the strip of threads is thus squeezed out. Downstream of the counter-rollers 42 a series of spray nozzles 44 of the washing water is inserted.
- the washing consists of an alternating sequence of imbibition and squeezing of the threads 1 in a strip to remove the residues of the alkaline mercerising solution, thus discharging the strip of threads washed through the deviating idle roller 28 arranged downstream of the drum 41B.
- the yarn is drawn as a consequence of the different linear actuation speed of the roller 30 and of the drum 41A, recovering the lost length through "shrinkage" and giving the definitive tension required to fully obtain the mercerising effects.
- the second washing stage is carried out in the container 40bis shown in figure 6 in its essential components, having the same structure and operations as the previous one, apart from the drawing function and the direction of the thread arriving from the previous stage. Therefore, the same reference numerals have been kept for the components present in the container 40bis.
- the motorisation of the shafts of the drums 41A, B is also controlled with independent actuation, for example through an inverter, given that the various angular speeds of the mercerising device are synchronised to obtain and keep coherent speeds within the device.
- the strip of threads 1 washed in the previous washing units is then subjected to neutralisation, for example with a diluted acetic or citric acid solution with pH of 2-2.5, inside the relative containers.
- neutralisation for example with a diluted acetic or citric acid solution with pH of 2-2.5, inside the relative containers.
- the neutralisation is shown in two stages: in the first neutralisation with acid is carried out, whereas in the second the final washing with water for greater purity is carried out.
- the neutralisation unit is totally analogous to the washing units and operates according to the same general scheme, apart from that the washing operates with water whereas neutralisation operates with acid solutions.
- 40 and 40bis plates 26, 46 for collecting the part of the various treatment fluids that is not held by the threads being treated are arranged, for its recovery and reuse, after a suitable reconditioning. As far as the washing waters are concerned, the criterion of countercurrent is used.
- the washing and neutralisation operations of the strip of threads 1 are thus carried out inside the containers 40 and 40bis with S-shaped paths around the drums 41A, B, on which an alternating sequence of imbibition and squeezing is carried out with the washing waters and with the acid solution, respectively.
- the strip of washed and neutralised threads 1 is then subjected to a drying and exsiccation stage, in the drying unit inside the container 60 shown in figure 7 in its essential components.
- the drying and exsiccation unit has an analogous structure to that of the treatment unit with alkaline solution.
- the strip of threads 1 is made to pass onto the surface of two rotary drums 61, heated with steam or with diathermal oil to suitable temperature.
- the strip of threads 1 is wound many times onto the hot surface of the drums 61 always with incomplete 8-shaped spirals.
- the deposit of the strip of threads 1 is regulated with the deviating rollers 62, totally analogous to the deviating rollers 24 of the container 5, also with a rotation axis oblique to the axes of the drums 61.
- the variation in inclination of the axes of the deviating rollers 62 allows the progressive axial gauge between the 8-shaped spirals that wind onto the drums 61 to be generated and allows their number to be varied, thus determining the length of the path of the strip of threads 1 and its time spent inside the exsiccation unit.
- the strip of threads 1 is discharged from the drying and exsiccation unit of the container 60 with one or more pairs of discharging rollers 64.
- a suction hood 65 for the vapours developed during the course of the drying and exsiccation of the threads takes these vapours away.
- the strip of threads 1 coming out from the exsiccation unit is then sent for the individual winding of each thread and does not require any particular operation to separate the threads 1 that make up the strip, since such threads have always kept their individuality.
- the winder 70 a series of reels 72 is produced that each contain one of the threads 1 that have been mercerised in the plant upstream.
- An important characteristic of the present invention is the way in which the threads make contact with the process fluids, alkaline solution, washing waters and neutralisation reagents, in the case of the mercerisation of cotton.
- the contact and the relative reactions are carried out by taking and feeding the process fluids directly to the single thread and avoiding the immersions in tanks or reactors of the prior art, which give a disadvantageous quantity ratio between the worked threads and the process fluids, In particular, the stage of reaction with the alkaline solutions takes place in a quite short time period.
- injector nozzles 12 in the imbibing device 8 which engage the threads 1 under treatment individually, injecting the alkaline solution under pressure, allows the mercerisation treatment to be completed in a time of around a tenth of a second and it does not require further reaction stages to achieve the desired result.
- the mercerisation process described up to now allows significant advantages compared to the processes of the prior art.
- the threads are worked as such and individually, without requiring them to firstly be joined in a package in an integral bundle, skeins or beams and later requiring their separation.
- the present invention allows work with good productivity since the strip of threads runs in the plant at a high speed going from the reels 2 and ending at the reels 72 for collecting the mercerised product.
- a further advantage lies in the small amount of fluids used and their greater yield, reducing the environmental implications.
- Processing with individual threads means that each of the threads 1 being treated goes from a reel 2 of index N in the creel 3 and reaches a reel 72 of index N.
- the winding head of index N indicates the absence of thread: it is quite simple and easy to indicate such an event to the creel 3 and consequently to thus automatically cause the relative end being fed to be cut and stop its winding head.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Treatment Of Fiber Materials (AREA)
- Chemical Or Physical Treatment Of Fibers (AREA)
Description
- The present invention refers to the mercerising treatment of cotton yarn to give them the desired characteristics for their end use to produce fabrics or other manufactured products. In textile technology the treatment of yarn with liquid reactants uses a large variety of processes, for the various types of fibres like cotton, wool, silk, linen and so on, with which the yarn is given the desired characteristics or undesired components that decrease its worth and its possibilities of use are removed from it. With reference to cotton, such treatment is typically mercerisation, but it can also concern other treatments like dyeing, bleaching and so on.
- In conventional industrial practice such treatment operations are generally carried out with discontinuous operations on discreet batches of yarn, which therefore must be suitably packed in reels or skeins, which after treatment must be unwound and repacked differently further on in the production line. Such discontinuous operations on the yarn are rather onerous and have problems due to the inconsistency in the quality of the product.
- The overriding tendency of technology development is therefore in the direction of continuous processing in the overall yarn production process. For continuous mercerising technology the Applicant is the owner of
European patent applications 1.369.519 ,1.369.520 and1.369.521 . In them it is foreseen to work many threads together, picking them up from their reels, bringing them together in an integral bundle and subjecting them together to the mercerising processing, separating them once again and winding them each in a reel. The contact between the bundle of yarn and the process fluids is carried out with a series of Venturi nozzles, in which the process fluids also act as driving fluid of the bundle of yarn in the contact apparatuses. From the aforementioned European patent applications it is possible to obtain further details on mercerising technology. - In the description of the present invention we refer to mercerisation, but explicitly stating that the system for continuously treating yarn according to the present invention can also have advantageous uses for different treatments to be carried out on yarn in textile technology.
- The mercerising treatment of cotton yarn improves its mechanical characteristics, improves it appearance, and enhances its absorption capacity and reactivity towards finishing products and the affinity towards dyes. In short, it consists of treating yarn with highly concentrated alkaline solutions followed by drawing and removal of the reactants with suitable washes. The treatment is carried out on individual fibres that make up the yarn in a semi-plastic state induced by the concentrated alkalis that imbibe them.
- In conventional technique the mercerisation is typically carried out on the yarn in skeins, prepared with a reeling stage, subjected to discontinuous mercerisation, and then washed, neutralised, dried, unwound and repacked in reels.
- In the prior art it has also been proposed to continuously treat yarn with mercerising solutions by first preparing the individual threads with winding in beams of hundreds of threads each. From such beams the threads are unwound in parallel, made to pass into a sequence of treatment baths, drawn by pairs of rollers and wound back up again.
- The most important prior art reference is constituted by
US 3,766,581 , disclosing a mercerising device operating on a bundle of yarns wound several times with incomplete 8-shaped spirals on one or more couples of horizontal parallel rotating rolls and an impregnating device which imbibes again and again the bundle of yarns at every passage of its 8-shaped spirals around the above rolls with the impregnating alkaline solution. Such impregnating device consists of two opposite plates having a series of grooves transversal to the motion of the bundle Y. The treating solution is sent in the middle of said plates and flows towards both lateral ends of the plates, flowing along the grooves. -
DE 41 21 593 discloses an impregnating device for treating thread, in which the thread circulates several times around one couple of vertical parallel rotating rolls having their bottom immersed into the treating medium. -
GB 960.150 - At the moment, such technical solutions have practically remained at the proposal stage due to the complications and the drawbacks that hinder its industrial practice. One of the requirements for industrial scale application of continuous mercerising techniques is the hourly productivity, in other words the ability to work a discreet number of threads simultaneously and with an acceptable speed, as productivity is linked to the product of these two parameters.
- The purpose of the present invention is to make a system for continuously treating yarn with process fluids, and specifically mercerisation, which allows the drawbacks of the systems used or proposed in the state of the art to be overcome.
- This purpose is accomplished according to the present invention with a mercerising process according to the more general definition of
claim 1 and, for preferred embodiments or possible variants,dependent claims 2 to 6. The present invention also makes it possible to make a device for continuously treating yarn, and in particular mercerisation, according toclaim 7 and the claims dependent upon it. - The characteristics and advantages of the present invention for continuously mercerising yarn, and more generally for continuously treating it with process fluids, can be seen more clearly from the following description thereof, given as a non-limiting example, referring to its application to the mercerisation of cotton, according to the plant scheme illustrated in
figure 1A .Figure 1B for the sake of greater clarity - transparently shows the perspective view of the apparatuses in which the overall mercerising treatment is carried out, for simplicity's sake omitting the initial creel and the final reel-winding frame. -
Figures 1A-B illustrate the general scheme of the system for continuously treating yarn with process fluids. -
Figure 2 and the detail offigure 2A illustrate the relevant details of the first device for imbibing the threads subjected to mercerisation.Figure 3 , on the other hand, illustrates the essential details of the container in which the mercerisation reaction takes place.Figure 4 on the other hand, illustrates the details of the hydro-extraction and drawing device after the mercerising reaction.Figure 5 then illustrates the details of thecontainer 40 in which the drawing of the yarn and its first washing with water take place.Figure 6 illustrates the containers 40bis in which both the second washing and the neutralisation stages take place. Finally,figure 7 illustrates the details of thecontainer 60 in which the drying and dehydration stage of the mercerised threads takes place. - In the general scheme of
figures 1A-B , theyarn 1 to be treated is fed from a series ofreels 2 arranged in parallel on acreel 3. Thereels 2 yield a plurality ofthreads 1, which are kept separate and parallel during the entire process and along the entire sequence of mercerising apparatuses. In order to carry out the process and make the device according to the invention on an industrial scale the processing must be carried out on a congruous number ofparallel threads 1, at least of the order of a few tens of threads at once, unwound with a speed at least of the order of 5-10 m/sec. - The return of the
parallel threads 1 is carried out with the pair ofmain guide rollers 4 with horizontal axis, which rotate at controlled speed and that determine the linear flow rate of the threads being processed taken to the mercerising unit, operating as outlined above at a linear speed of at least 5-10 m/sec. - A relevant characteristic of the present invention lies in the operation of the treatment and in the structure of the mercerising reactor in which the treatment of the threads is carried out with sodium hydroxide alkaline solution. Such an operation is carried out in a closed parallelepiped-
shaped container 5. Inside the closedcontainer 5, in general shaped like a wardrobe that can be opened for the intervention of operators, it is possible to maintain a controlled atmosphere, just like for the other further containers foreseen in the unit. On its inside, the group ofparallel threads 1 is deviated and guided firstly withrollers 7 with horizontal axis and worked with radial grooves that allow the threads to be kept separate and spaced apart during the entire mercerising reaction. - The strip of parallel and
separated threads 1 is fed to a firstimbibing device 8 illustrated in greater detail infigure 2 , which shows plan, front and side section views. It consists of animbibing plate 10 equipped withlongitudinal grooves 11 that are independent and have constant pitch, which guide thethreads 1 separately. The mercerising fluid consists of the alkaline solution, for example sodium hydroxide at 30° Be, and is sprayed on theplate 10 withsprayers 12 with nozzles at thegrooves 11 in which thethreads 1 run at a speed controlled by theinitial guide rollers 4. The top part of thegrooved plate 10 is protected with acover 13. - According to a preferred embodiment of the invention, at the entry of the strip of
threads 1 into the imbibing device 8 asealing device 15 is arranged. It consists of anelongated tank 16, fed with the same mercerising solution and kept at atmospheric pressure, with a lower slit that comes out onto the grooves that guide and contain the threads in movement from left to right in the drawing according to the arrows F. The liquid head of thetank 16 allows a first imbibition at atmospheric pressure of thethreads 1 and avoids the entry of air into the second treatment area with the pressurised solution. In this second area theplate 10 is worked with V-shaped grooves, whereas thecover 13 is provided with one ormore sprayers 12 consisting of a series ofpressurised injection micro-nozzles 18, shown in the detail offigure 2A and each arranged at eachindividual groove 11 crossed by a single thread. Eachsprayer 12 and thetank 16 are fed withfittings 17 from a general feeding duct, not shown in the figures, which takes the alkaline mercerising solution at constant pressure and at controlled temperature. - The temperature of the mercerising solution is kept at 30-35°C, whereas the injection overpressure is between 1 and 15 bars, preferably between 1.5 and 4 bars. Indeed, it has been found that the injection overpressure of the mercerising fluid causes a substantial increase in the mercerisation reaction kinetics, which can be attributed to a better exchange coefficient and a more efficient contact between the liquid phase and cellulose micelles, substantially accelerating the mercerising reaction. In conventional mercerisation techniques by immersion in baths or recipients at atmospheric pressure contact times of the order of minutes are required, whereas the technical solution according to the present invention allows such contact times to be drastically reduced, reducing them to the order of magnitude of 10 seconds.
- Again inside the
container 5, the strip ofthreads 1, after imbibition in thedevice 8, then passes onto the surface of tworotary drums 20, on which the strip ofthreads 1 is wound many times with incomplete 8-shaped spirals 21, whereas inside of them the mercerising reaction takes place between the imbibing solution and the cellulose. - The structure and the operation of the
rotary drums 20 and of the other elements inside thecontainer 5 is illustrated in greater detail infigure 3 , in which they are shown in perspective view and transparently. Thedrums 20 are mounted parallel with substantially horizontal axis and they are equipped with a substantially smooth cylindrical surface. The incomplete 8-shaped spirals 21 are deposited on the surface of thedrums 20. The deposit of the strip ofthreads 1 is guided withrotary combs 22, made up of a series of grooved ceramic bushings mounted with constant pitch on a shaft, and with the deviatingrollers 24. The deviatingrollers 24 have a substantially smooth surface, they are mounted with oblique rotation axis with respect to the axes of thedrums 20 and they are equipped with means for varying their inclination. The inclination to the right or left of the axes of the deviatingrollers 24 allows the progressive axial gauge between the 8-shaped spirals that wind on thedrums 20 to be determined. Again with reference tofigure 3 , the whole of thethreads 1 in a strip enters into the rear part at themain guide rollers 4, passes theimbibing device 8, winds - starting from the right-hand drum 20 - with 8-shaped spirals that advance towards the front part of thecontainer 5, and discharges - from the left-hand drum 20 - through the hydro-extraction anddrawing device 27. In the path betweenimbibing device 8 to the hydro-extraction device 27 the mercerising reaction between the cellulose micelles of the yarn and the solution that imbibes the yarn itself takes place. - The variation in inclination of the axes of the deviating
rollers 24 allows the progressive axial gauge to be generated between the 8-shaped spirals that wind on thedrums 20 and allows the number of spirals that can be carried by the available length of thedrums 20 to be varied, thus determining the length of the path of the strip ofthreads 1 and its treatment time with alkaline solution. For example, with substantially "square"cylindrical drums 20, with a diameter and length of about 1000 mm, it is possible to wind 50-100 m of strip ofthreads 1 and to carry out reaction times within the range of 8-15 seconds, which corresponds to the time of complete "re-entry", in other words the time for completion of the reactions between the cellulose and the alkaline solution, which result in the shortening of the yarn by values of 10-20% according to the type of yarn and the original cotton. - In the space contained between the two
drums 20, i.e. in the free parts of thespirals 21 of the strip ofthreads 1, one or more series of further spray nozzles is arranged close to the surface of the drums themselves, to renew the contact between yarn and alkaline solution. - Such spray nozzles are placed on nozzle-carrying
rods 25 and are analogous to those that equip theimbibing device 8, but operating at lower pressure, and the position of a pair ofrods 25 thereof is shown as an example infigure 1A . - At the end of the path inside the
container 5 for treatment with alkaline solution, the strip ofthreads 1 is discharged with the hydro-extraction anddrawing device 27 after the mercerising reaction. It is shown infigure 4 with its essential components. The strip ofmercerised threads 1 still imbibed with alkaline solution passes fromidle deviating rollers 28 and reaches the hydro-extraction device 29 consisting of amotorised roller 30 against which twoidle counter-rollers 31 are pressed, preferably made from polymeric elastic material. Such aroller 30 rotates at the linear speed of the strip ofthreads 1 fed, decreased by the expected percentage shrinkage for the mercerisation. In the part of the strip ofthreads 1 between the last spiral around the left-hand drum 20 and thedevice 27 the so-called shrinkage of the threads therefore takes place. In the contact between said rollers the alkaline solution still present in the threads is hydro-extracted and to a large extent recovered. The whole of theroller 30 and the counter-rollers 31 also acts as a seal against the shrinkage of the strip of threads hydro-extracted by therotary drums 41A, B of the washing section arranged downstream, which operate at higher linear speeds than that of theroller 30. Such shrinkage generates the drawings of the mercerised yarn, tending both to recover the shrinkage undergone during the mercerisation step and to further stretch the threads of the strip, thus giving them the positive characteristics that derive from the mercerisation. - All of the motorisations of the shafts of the rotary members inside the
container 5, in other words thedrums 20, the rotary combs 22, the deviatingrollers 24 and theroller 30, are controlled with independent actuations, for example through inverters, and the various angular speeds are synchronised with each other to obtain and keep the linear speeds for thedrums 20 and the deviatingrollers 24 coherent with that of the strip ofthreads 1 being processed. The rotation speed of thecombs 22, on the other hand, is lower (2-10 revolutions per minute); it is carried out to limit the erosion phenomena of the ceramic bushes of which they consist. - According to a preferred embodiment of the invention, a
device 35 for capturing the ends of the threads that have broken is arranged at themotorised roller 30 of the hydro-extraction device 29. Indeed, there is greater probability of breaking at the drawing of the mercerised threads and, in this case, the ends tend to stick and wind onto theroller 30. - The
device 35, for example, can consist of asuction mouth 36 connected to asuction duct 37; the top edge of its suction slit 38 is made from polymeric material and is arranged to scrape the metallic surface of theroller 30. In this way, the possible end that winds onto the surface of said roller is stopped and sucked up by themouth 36. Alternatively, thedevice 35 for capturing the ends can be made with a rotary brush of bristles made from polymeric material that, mounted in the same position as themouth 36 and made to rotate at a high speed, clears theroller 30 of the possible ends that would otherwise wind onto its surface. - After passing into the
container 5 in which the contact is made between thethreads 1 in a strip and the alkaline mercerising solution, said strip is fed for washing with water. For example, the washing can be carried out in many stages with water in countercurrent and at decreasing temperature, according to methods already known in the field. - The first washing stage is carried out in the
container 40, illustrated infigure 5 with its essential components. In it the washing operation of the yarn treated with the alkaline solution and coming from thecontainer 5 takes place. The strip ofthreads 1 is guided and deviated by a series ofidle rollers 28 up to the rotarycylindrical drums 41A, B made from metallic material and with a smooth surface. The strip of threads is inserted and held between the surface of thedrums 41A, B and a series of idle cylindrical counter-rollers 42 that wrap around them and are kept pressed to grip said strip. At each passage under such counter-rollers the liquid contained by the strip of threads is thus squeezed out. Downstream of the counter-rollers 42 a series ofspray nozzles 44 of the washing water is inserted. The washing consists of an alternating sequence of imbibition and squeezing of thethreads 1 in a strip to remove the residues of the alkaline mercerising solution, thus discharging the strip of threads washed through the deviatingidle roller 28 arranged downstream of thedrum 41B. As already stated, in passing from theroller 30 of the squeezinggroup 29 to the contact betweendrum 41A and thefirst counter-roller 42 of the first washing unit in thecontainer 40 the yarn is drawn as a consequence of the different linear actuation speed of theroller 30 and of thedrum 41A, recovering the lost length through "shrinkage" and giving the definitive tension required to fully obtain the mercerising effects. - The second washing stage is carried out in the container 40bis shown in
figure 6 in its essential components, having the same structure and operations as the previous one, apart from the drawing function and the direction of the thread arriving from the previous stage. Therefore, the same reference numerals have been kept for the components present in the container 40bis. - The motorisation of the shafts of the
drums 41A, B is also controlled with independent actuation, for example through an inverter, given that the various angular speeds of the mercerising device are synchronised to obtain and keep coherent speeds within the device. - The strip of
threads 1 washed in the previous washing units is then subjected to neutralisation, for example with a diluted acetic or citric acid solution with pH of 2-2.5, inside the relative containers. In the embodiment illustrated here, again for illustrating and not limiting purposes, the neutralisation is shown in two stages: in the first neutralisation with acid is carried out, whereas in the second the final washing with water for greater purity is carried out. The neutralisation unit is totally analogous to the washing units and operates according to the same general scheme, apart from that the washing operates with water whereas neutralisation operates with acid solutions. It corresponds to the scheme offigure 6 in terms of its components and the path of the strip ofthreads 1, feeding with a pressurised flow of a diluted acetic or citric acid solution to remove the alkaline residue from thethreads 1 of the strip that comes out from the previous washing. In the container 40bis offigure 6 the same reference numerals refer to components that are similar and have the same function as thecontainer 40 offigure 5 . - In the bottom part inside the
container plates - The washing and neutralisation operations of the strip of
threads 1 are thus carried out inside thecontainers 40 and 40bis with S-shaped paths around thedrums 41A, B, on which an alternating sequence of imbibition and squeezing is carried out with the washing waters and with the acid solution, respectively. - The strip of washed and neutralised
threads 1 is then subjected to a drying and exsiccation stage, in the drying unit inside thecontainer 60 shown infigure 7 in its essential components. - The drying and exsiccation unit has an analogous structure to that of the treatment unit with alkaline solution. The strip of
threads 1 is made to pass onto the surface of tworotary drums 61, heated with steam or with diathermal oil to suitable temperature. The strip ofthreads 1 is wound many times onto the hot surface of thedrums 61 always with incomplete 8-shaped spirals. The deposit of the strip ofthreads 1 is regulated with the deviatingrollers 62, totally analogous to the deviatingrollers 24 of thecontainer 5, also with a rotation axis oblique to the axes of thedrums 61. The variation in inclination of the axes of the deviatingrollers 62 allows the progressive axial gauge between the 8-shaped spirals that wind onto thedrums 61 to be generated and allows their number to be varied, thus determining the length of the path of the strip ofthreads 1 and its time spent inside the exsiccation unit. The strip ofthreads 1 is discharged from the drying and exsiccation unit of thecontainer 60 with one or more pairs of dischargingrollers 64. Asuction hood 65 for the vapours developed during the course of the drying and exsiccation of the threads takes these vapours away. - The strip of
threads 1 coming out from the exsiccation unit is then sent for the individual winding of each thread and does not require any particular operation to separate thethreads 1 that make up the strip, since such threads have always kept their individuality. In the winder 70 a series ofreels 72 is produced that each contain one of thethreads 1 that have been mercerised in the plant upstream. - An important characteristic of the present invention is the way in which the threads make contact with the process fluids, alkaline solution, washing waters and neutralisation reagents, in the case of the mercerisation of cotton. The contact and the relative reactions are carried out by taking and feeding the process fluids directly to the single thread and avoiding the immersions in tanks or reactors of the prior art, which give a disadvantageous quantity ratio between the worked threads and the process fluids, In particular, the stage of reaction with the alkaline solutions takes place in a quite short time period. The use of the
injector nozzles 12 in theimbibing device 8, which engage thethreads 1 under treatment individually, injecting the alkaline solution under pressure, allows the mercerisation treatment to be completed in a time of around a tenth of a second and it does not require further reaction stages to achieve the desired result. - The mercerisation process described up to now allows significant advantages compared to the processes of the prior art. In addition to the advantage of carrying out the treatment with continuous operations, it is significant that the threads are worked as such and individually, without requiring them to firstly be joined in a package in an integral bundle, skeins or beams and later requiring their separation. The present invention allows work with good productivity since the strip of threads runs in the plant at a high speed going from the
reels 2 and ending at thereels 72 for collecting the mercerised product. - A further advantage lies in the small amount of fluids used and their greater yield, reducing the environmental implications. Processing with individual threads means that each of the
threads 1 being treated goes from areel 2 of index N in thecreel 3 and reaches areel 72 of index N. In the case in which a thread breaks along the path, in thewinder 70 the winding head of index N indicates the absence of thread: it is quite simple and easy to indicate such an event to thecreel 3 and consequently to thus automatically cause the relative end being fed to be cut and stop its winding head.
Claims (10)
- Process for continuously mercerising cellulose yarn (1) comprising treatment of the yarn with alkaline solution, of drawing the yarn, the aqueous washing and the neutralisation of the residue of alkalinity still present in the yarn, starting from starting reels (2) of yarn and to produce finished reels (72) of mercerised yarn, the process being carried out continuously on a plurality of threads (1) along the entire mercerising apparatus, and in that the process fluids are fed directly to the threads (1) without immersion in treatment baths, said yarns being moved from the starting reels (2) to the finished reels (72), the threads (1) being firstly subjected to imbibition with alkaline solution in an imbibing device (8) and then pass onto the surface of rotary drums (20), being wound many times with incomplete 8-shaped spirals (21), thus determining with the number of spirals the length of the path of threads (1) and its treatment time with alkaline solution, whilst the mercerising reaction between the imbibing solution and the cellulose mixtures takes place inside of them, characterized in that the threads (1) are in strip, kept separate and spaced apart during the entire mercerizing reaction, and further characterised in that the imbibition of the threads (1) is carried out avoiding the entry of air, with a series of pressurised injector micro-nozzles (18), each arranged at a longitudinal groove (11) crossed by a single thread (1), the longitudinal grooves (11) so guiding the threads (1) inside, separately and at high speed.
- Process for mercerising yarn according to claim 1, characterised in that the injection overpressure in the micro-nozzles (18) is between 1 and 15 bars, and preferably between 1.5 and 4 bars.
- Process for mercerising yarn according to claim 1, characterised in that between the drums (20), in the free parts of the spirals (21) of the strip of threads (1), the contact between yarn and alkaline solution is renewed with further spray nozzles arranged on nozzle-carrying rods (25).
- Process for mercerising yarn according to claim 1, characterised in that at the end of the treatment with alkaline solution the strip of threads (1) is removed with a roller (30) rotating at the linear speed of the strip of threads (1) being fed, decreased by the expected percentage shrinkage for the mercerisation, thus allowing the threads to shrink in the part of free strip of threads (1) between the last spiral and the roller (30).
- Process for mercerising yarn according to claim 1, characterised in that the washing and neutralisation treatments are carried out by winding the strip of threads (1) with S-shaped paths about rotary drums (41A, B) on which an alternating imbibition and hydro-extraction sequence takes place with washing water and with acid solution, respectively.
- Process for mercerising yarn according to claim 4 and 5, characterised in that in passing from the roller (30) to the drum (41A) and the first counter-roller (42) of the first washing unit the drawing of the yarn takes place as a result of the different linear actuation speed of the roller (30) and the drum (41A).
- Device for continuously mercerising cellulose yarn comprising devices for treating the yarn with alkaline solution, for drawing the yarn, for aqueous washing and neutralisation of the residue of alkalinity still present in the yarn, starting from starting reels (2) of yarn and to produce finished reels (72) of mercerised yarn, such devices operating continuously on a plurality of threads (1) along the entire mercerising apparatus, feeding the process fluids directly to the threads (1) without immersion in treatment baths, and comprising an imbibing device (8) with alkaline solution and two rotary drums (20), on which the strip of threads is wound many times with incomplete 8-shaped spirals (21), thus determining the length of the path along which the mercerising reaction between the imbibing solution and the cellulose micelles takes place, characterized in that the device comprises means (7) to allow the threads (1) to be kept separate and spaced apart during the entire mercerizing reaction, and further characterised in that the imbibing device (8) consists of an imbibing plate (10) equipped with independent longitudinal grooves (11), which separately guide inside a single thread (1), and on which the alkaline solution is sprayed with sprayers (12) with micro-nozzles (18) each arranged at longitudinal grooves (11) in which the thread (1) runs, the top part of the groove plate (10) being protected by a cover plate (13).
- Device for continuously treating yarn with process fluids according to claim 7, characterised in that the two rotary drums (20) are provided with means for determining the gauge of the incomplete 8-shaped spirals, and for varying the number of spirals that can be carried by the available length of the drums (20), thus determining the length of the path of the strip of threads (1) and its treatment time with alkaline solution.
- Device for continuously treating yarn with process fluids according to claim 7, characterised in that at the entry of the strip of threads (1) into the imbibing device (8) a sealing device (15) is arranged consisting of a tank (16), fed with the same mercerising solution, with a lower slit that comes out onto the grooves (11) that gives a liquid head at the start of said grooves and a first impregnation of the threads (1).
- Device for continuously treating yarn with process fluids according to claim 8, characterised in that the means for determining the gauge of the spirals wound on the rotary drums (20) consist of deviating rollers (24) mounted with oblique rotation axis with respect to the axes of the drums (20) and equipped with means for varying their inclination, to generate the progressive axial gauge between the incomplete 8-shaped spirals that wind on the drums (20).
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| ITMI20061767 ITMI20061767A1 (en) | 2006-09-15 | 2006-09-15 | PROCEDURE AND DEVICE FOR CONTINUOUS MERCERIZATION OF TEXTILE YARNS |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1900864A2 EP1900864A2 (en) | 2008-03-19 |
| EP1900864A3 EP1900864A3 (en) | 2009-08-05 |
| EP1900864B1 true EP1900864B1 (en) | 2011-03-30 |
Family
ID=38829569
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20070115878 Active EP1900864B1 (en) | 2006-09-15 | 2007-09-07 | Process and device for continuously mercerising spun yarn |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP1900864B1 (en) |
| CN (1) | CN101144235B (en) |
| DE (1) | DE602007013500D1 (en) |
| IT (1) | ITMI20061767A1 (en) |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101525826B (en) * | 2009-03-10 | 2012-05-09 | 东华大学 | A method for continuous reflow mercerizing of yarn bundles |
| ITMI20121360A1 (en) * | 2012-08-01 | 2014-02-02 | Reggiani Macchine Spa | MACHINE AND METHOD FOR THE MERCERISATION OF YARNS OR FABRICS |
| ITMI20121361A1 (en) * | 2012-08-01 | 2014-02-02 | Reggiani Macchine Spa | MACHINE FOR MERCERIZATION OF YARNS |
| CN110011226B (en) * | 2019-03-29 | 2024-12-03 | 北京理工大学 | Wiring device |
| CN113403764B (en) * | 2021-07-02 | 2024-01-09 | 台嘉蚌埠玻璃纤维有限公司 | Wire drawing machine capable of automatically flushing and flushing method |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2292629A (en) * | 1939-08-12 | 1942-08-11 | American Rayon Company Inc | Method for imparting finish to cotton yarn |
| GB960150A (en) * | 1963-04-11 | 1964-06-10 | Inst Textilmaschinen | Improvements in or relating to apparatus for sizing warp threads |
| GB1268376A (en) * | 1968-06-06 | 1972-03-29 | Stone Platt Crawley Ltd Former | Improvements relating to conveyors |
| US3864949A (en) * | 1970-08-05 | 1975-02-11 | Kanegafuchi Spinning Co Ltd | Apparatus for continuously treating thread |
| US3766581A (en) * | 1970-08-05 | 1973-10-23 | Kanegafuchi Spinning Co Ltd | Process for continuously treating thread |
| DE4121593A1 (en) * | 1991-06-29 | 1993-01-07 | Croon Lucke Maschinen | DEVICE FOR CONTINUOUSLY TREATING YARNS IN FLUID MEDIA |
| FR2739880B1 (en) * | 1995-10-13 | 1997-12-05 | Superba Sa | CONTINUOUS YARN DYING PROCESS, IN PARTICULAR BASED ON CELLULOSIC FIBERS WITH REACTIVE DYES, AND DEVICE FOR IMPLEMENTING THIS PROCESS |
| ITMI20021220A1 (en) * | 2002-06-05 | 2003-12-05 | Savio Macchine Tessili Spa | PROCEDURE AND DEVICE FOR THE CONTINUOUS MARKETING OF TEXTILE YARNS |
| ITMI20021221A1 (en) | 2002-06-05 | 2003-12-05 | Savio Macchine Tessili Spa | DEVICE FOR THE CONTINUOUS TREATMENT OF YARNS WITH PROCESS FLUIDS |
| ITMI20021223A1 (en) | 2002-06-05 | 2003-12-05 | Savio Macchine Tessili Spa | CONTINUOUS YARN TREATMENT SYSTEM WITH PROCESS FLUIDS PARTICULARLY FOR THEIR MARKETING UNDER VOLTAGE |
-
2006
- 2006-09-15 IT ITMI20061767 patent/ITMI20061767A1/en unknown
-
2007
- 2007-09-07 DE DE200760013500 patent/DE602007013500D1/en active Active
- 2007-09-07 EP EP20070115878 patent/EP1900864B1/en active Active
- 2007-09-14 CN CN2007101536904A patent/CN101144235B/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| ITMI20061767A1 (en) | 2008-03-16 |
| DE602007013500D1 (en) | 2011-05-12 |
| EP1900864A3 (en) | 2009-08-05 |
| EP1900864A2 (en) | 2008-03-19 |
| CN101144235A (en) | 2008-03-19 |
| CN101144235B (en) | 2012-11-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1900864A2 (en) | Process and device for continuously mercerising spun yarn | |
| EP3152358B1 (en) | Method for dyeing and finishing textile material and corresponding apparatus | |
| IL44523A (en) | Machines for continously spinning and treating rayon-viscose filaments and yarns | |
| US2367730A (en) | Textile dyeing and finishing, method and product | |
| US4416124A (en) | Sheet-dyeing apparatus | |
| EP1369521B1 (en) | Process for the continuous mercerizing of textile yarns | |
| US7090702B2 (en) | Continuous treatment system of yarns with process fluids, particularly for their mercerization under tension | |
| US3766581A (en) | Process for continuously treating thread | |
| EP0489191A1 (en) | Method for continuous mercerising, and apparatus that employs such method | |
| US4376632A (en) | Process and plant for the continuous mercerization of raw or colored open or tubular knitted fabric | |
| US3643474A (en) | Apparatus for wet treating textile fabrics | |
| DE4218551A1 (en) | Continuous yarn bundle processing - in which bundle is held at a constant length in caustic soda or mercerising fluid to be mangled and neutralised | |
| US7140207B2 (en) | Device for the continuous treatment of yarns with process fluids | |
| EP1106725A2 (en) | Machine for continuously washing and finishing fabrics or the like | |
| US4263008A (en) | Method and apparatus for continuously carrying out weight reduction and mercerization of cloth material | |
| US2139017A (en) | Process for producing filaments like horsehair | |
| JPS5953940B2 (en) | Continuous cleaning method for textiles | |
| DE2527450A1 (en) | Yarn dyeing device - formed by hermetically sealed housing enclosing a winding device and dyeing media supply lines terminating adjacent wound bobbin | |
| US3864949A (en) | Apparatus for continuously treating thread | |
| IT8983488A1 (en) | CONTINUOUS MERCERIZATION PROCEDURE AND EQUIPMENT ADOPTING THIS PROCEDURE | |
| DE723363C (en) | Method and device for the production of cottonized fibers from bast fibers in tape form | |
| EP0977916A1 (en) | Erfahren und anlagu | |
| GB391863A (en) | Improvements in or relating to the treatment and manufacture of artificial yarns, threads, filaments and the like | |
| DE2116C (en) | Process for straightening and finishing yarns | |
| KR920006472B1 (en) | Scouring method for cotton fabric and system therefor |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK YU |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: CEOLIN, MAURO Inventor name: MINUTI, MARIO Inventor name: QUAIA, AMEDEO Inventor name: BADIALI, ROBERTO |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK RS |
|
| 17P | Request for examination filed |
Effective date: 20100114 |
|
| 17Q | First examination report despatched |
Effective date: 20100208 |
|
| AKX | Designation fees paid |
Designated state(s): CH DE IT LI TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE IT LI TR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 602007013500 Country of ref document: DE Date of ref document: 20110512 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602007013500 Country of ref document: DE Effective date: 20110512 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: PATENTANWAELTE SCHAAD, BALASS, MENZL & PARTNER AG |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20120102 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602007013500 Country of ref document: DE Effective date: 20120102 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 602007013500 Country of ref document: DE Representative=s name: SCHWABE SANDMAIR MARX, DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PFA Owner name: SAVIO MACCHINE TESSILI S.P.A., IT Free format text: FORMER OWNER: PENELOPE S.P.A., IT Ref country code: CH Ref legal event code: PFUS Owner name: PENELOPE S.P.A., IT Free format text: FORMER OWNER: SAVIO MACCHINE TESSILI S.P.A., IT Ref country code: CH Ref legal event code: PUE Owner name: MARIO MINUTI, IT Free format text: FORMER OWNER: SAVIO MACCHINE TESSILI S.P.A., IT |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 602007013500 Country of ref document: DE Representative=s name: SCHWABE SANDMAIR MARX, DE Effective date: 20130624 Ref country code: DE Ref legal event code: R081 Ref document number: 602007013500 Country of ref document: DE Owner name: MINUTI, MARIO, IT Free format text: FORMER OWNER: SAVIO MACCHINE TESSILI S.P.A., PORDENONE, IT Effective date: 20130624 Ref country code: DE Ref legal event code: R082 Ref document number: 602007013500 Country of ref document: DE Representative=s name: SCHWABE SANDMAIR MARX PATENTANWAELTE RECHTSANW, DE Effective date: 20130624 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230523 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20240927 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20241002 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20250822 Year of fee payment: 19 Ref country code: IT Payment date: 20250908 Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: H13 Free format text: ST27 STATUS EVENT CODE: U-0-0-H10-H13 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260425 |