EP0719706B1 - Beschickungsvorrichtung für Kartons und Verfahren zum Betreiben einer Beschickungsvorrichtung - Google Patents
Beschickungsvorrichtung für Kartons und Verfahren zum Betreiben einer Beschickungsvorrichtung Download PDFInfo
- Publication number
- EP0719706B1 EP0719706B1 EP95115012A EP95115012A EP0719706B1 EP 0719706 B1 EP0719706 B1 EP 0719706B1 EP 95115012 A EP95115012 A EP 95115012A EP 95115012 A EP95115012 A EP 95115012A EP 0719706 B1 EP0719706 B1 EP 0719706B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- magazines
- carton blanks
- carton
- engaging
- suction cup
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 19
- 238000004026 adhesive bonding Methods 0.000 claims description 7
- 238000007493 shaping process Methods 0.000 claims 3
- 230000008569 process Effects 0.000 description 8
- 239000003795 chemical substances by application Substances 0.000 description 6
- 230000008901 benefit Effects 0.000 description 3
- 230000008859 change Effects 0.000 description 2
- 239000003292 glue Substances 0.000 description 2
- 230000037431 insertion Effects 0.000 description 2
- 238000003780 insertion Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 238000004806 packaging method and process Methods 0.000 description 2
- 238000012858 packaging process Methods 0.000 description 2
- 230000004913 activation Effects 0.000 description 1
- 230000009849 deactivation Effects 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 230000002452 interceptive effect Effects 0.000 description 1
- 238000012856 packing Methods 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H3/00—Separating articles from piles
- B65H3/44—Simultaneously, alternately, or selectively separating articles from two or more piles
- B65H3/446—Simultaneously, alternately, or selectively separating articles from two or more piles alternatively, i.e. according to a fixed sequence
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/12—Feeding flexible bags or carton blanks in flat or collapsed state; Feeding flat bags connected to form a series or chain
- B65B43/14—Feeding individual bags or carton blanks from piles or magazines
- B65B43/145—Feeding carton blanks from piles or magazines
Definitions
- the inventions relate to a loading device for boxes with at least two for one Receiving and delivering trained cardboard blanks Magazines are used, and taking the cardboard blanks the cardboard blanks via a gripping means forming machine and glueing the cardboard blanks are supplied, and on the other hand a method for Operating such a loading device.
- the inventions are based on the tasks, one Carton loading device and method for Operating such a feed system to find that a trouble-free and immediate insertion or modification a certain alternation order for different printed cardboard blanks, even while it is running Packaging process, is possible.
- a sorting process should also be carried out of differently printed cardboard blanks together with the subsequent filling of the sorted Cardboard blanks in a magazine are not required.
- the magazines are rigid with each other connected to achieve the supply of a Magazine at the same time removing another magazine causes.
- the route also runs perpendicular to the direction of movement of the means gripping the cardboard blanks so that the Displacement distances are minimal and the gripping means normal on a surface of a cardboard blank can attack.
- the loading device according to the invention and that Methods according to the invention also have the advantage that a problem-free and immediate insertion or modification of one certain alternation order for different printed cardboard blanks, even while it is running Packaging process, is possible.
- Each magazine is printed differently Cardboard blanks equipped.
- the magazines moved so that either after each Removing a cardboard blank from a magazine other magazine is moved to the position at which the gripping agent grabs a cardboard blank again.
- a magazine remains in the for several gripping processes Position in which it supplies the gripping agent and then another magazine with cardboard blanks is cut with a different print in which the gripping medium supply position pushed and lingers there for the Duration of the same number of gripping processes.
- a loading device on at least one Ball roller bushing to store (claim 2) has the advantage that the frictional forces when moving the loading device are minimized, and thus moving the loading device relatively smooth and done quickly.
- the same advantages are in use a pneumatic cylinder as a drive for the magazines (Claim 3) given.
- Claim 4 Is analogous to the means that grips the cardboard blanks Claim 4 provided at least one suction cup, so is a reliable and proven gripping agent used.
- the suction cup can either by pressing it against a vacuum cut to a carton cut Grab a box cut, pass it on and detach itself from the cardboard blank by traction, or but the performance of a suction cup is supported.
- Claim 5 can be a larger suction cup Apply holding force when using a vacuum source connected is. A vacuum created on the suction cup increases also the reliability of the interfering means.
- the Suction cup connected to a compressed air source claim 6
- Means of Activation and deactivation of the suction cup from the Vacuum source or compressed air source allow one Precise use of vacuum and compressed air.
- One optimal use is obtained if, according to claim 7 intermittently with each gripping process the suction cup as gripping agent first with the vacuum source, for gripping of the cardboard blank, and then with the compressed air source to Detaching the cardboard blank from the gripping means, connects.
- the magazines will be removed after each removal moved, so boxes are alternately with different printing.
- the packaging system is thus filled and closed Cardboard boxes with alternating printing.
- These filled Cartons are created in the order in which they are created were placed in rows in collection containers, for example trays or packed large boxes.
- the Collection boxes the boxes of different printing in alternating order.
- the method can be chosen so that the magazines according to each removal of a large number of cardboard blanks be moved. This makes it possible to alternate boxes each with several similarly printed boxes generate one after the other. For example, uniform printed rows of boxes in a collection container are generated, with adjacent rows different are printed if the magazines after a large number of cardboard blanks moved will, and this large number of boxes per Row of boxes in a collection container corresponds. Corresponds to the multitude of the number of boxes in a collection container (Claim 9), so individual containers can each filled with boxes of the same printed image, and successive collection containers contain boxes with different print image.
- the loading device can cut cardboard to a Pass box forming device (claim 11).
- a Pass box forming device (claim 11).
- the folding arm pushes an incoming one Cardboard cut into a folding form and thereby forms one Carton.
- After a cut to the box beforehand applied layer of glue is the cardboard blank in the Folded form also pressed on the glued areas and thus glued.
- the folding arm works intermittently. After Once the open carton has been filled, it will be filled finally sealed and fed to a case packer.
- the gripping agent can also cut carton blanks in the direction pass on a conventional case erector (claim 12).
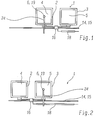
- the loading device 1 has two magazines 2, 3 with cardboard blanks 4, 5 stacked therein (FIG. 1). On a magazine 2 lies towards and from the magazine 2 this moving, gripping means 6.
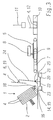
- the gripping means 6 grips a cardboard blank 4 from the Magazine 2 and passes this cardboard blank 4 on to Conveyor belt 7 ( Figure 3).
- Conveyor belt 7 Via the conveyor belt 7 Cardboard blank 4 under a gluing device 8 passed by. From the nozzles 9 of the gluing device 8 The glue released wets the linear areas the cardboard blank 5, which are to be glued.
- the Conveyor belt 7 conveys the cardboard blank 4 to one Folding form 10, where the glued cardboard blank then by means of a folding arm 11 is pressed into the folding form 10.
- the cardboard blank 4 becomes a glued cardboard 12 shaped.
- the contact pressure of the folding arm 11 in the folded form 10 is used both for deforming or buckling the Carton blank 4, as well as for pressing on gluing surfaces of the cardboard blank 4 required.
- the box 12 After leaving the one acting as box forming device 13 Folded form 10, the box 12 is filled, closed and finally fed to a collection container.
- the other magazine 3 the gripping means 6 pushed up ( Figure 2), so alternately from the two magazines 2, 3 Cardboard blanks 4, 5 are removed.
- Each of the two Magazine 2, 3 contains a stack of cardboard blanks 4, 5 with a uniform print image on the cardboard blank 4, 5.
- One magazine 2 contains cardboard blanks 4 a different print image than the cardboard blanks 5 of the Magazine 3.
- the magazines 2, 3 are rigidly connected to one another (FIG 1, Figure 2). You will be along a straight route 14 forming rod 15 moved. Route 14 runs thereby at a right angle to the direction of movement of the the cardboard blanks 4, 5 engaging means 6.
- the magazines 2, 3 are on the rod 15 on one Ball roller bushing 16 mounted. This is a shift of magazines 2, 3 possible with low friction.
- As Drive 17 for magazines 2, 3 is a pneumatic one Cylinder 18 provided.
- a suction cup 19 is attached to the gripping means 6, who grips a cardboard blank 4, 5 by means of negative pressure and takes from a magazine 2, 3 ( Figure 3).
- the suction cup 19 is connected to a vacuum source 21 via a pipeline 20 connected.
- the vacuum of the vacuum source 21 is too Suction cup 19 can be switched on and off.
- Another one Pipeline 22 is the suction cup 19 with an additional Compressed air source 23 connected.
- the overpressure of the Compressed air source 23 is also to suction cup 19 feedable or can be interrupted towards the suction cup 19 will.
- the gripping means 6 works in such a way that it cyclically with each gripping process first with the vacuum source 21 is connected and thereby a cardboard blank 4, 5 engages by means of negative pressure.
- the loading device 1 can in various ways and Operated in a manner. To generate a series of Cardboard boxes 12 with alternating printing on two Cartons 12 produced in close succession are the Magazines 2, 3 immediately after each removal of a cardboard blank shifted. To generate each a large number of boxes 12 with the same printing and then generating the same plurality Cardboard boxes 12 with different printing will be the loading device for the number corresponding to this multitude on removal of cardboard blanks 4, 5 in the in FIG Leave position shown and then in a Position shifted analogous to Figure 2, in which the Feeder 1 for the same number Withdrawals remain.
- This number corresponds to the number of Cardboard boxes 12 in a cardboard row of a collecting container or even the whole itself in a collection container located cartons 12, rows of the same type Cartons 12 are fed to a collection container and thus Rows of differently printed boxes 12 in Collection containers are generated, or a collection container can only be provided with boxes 12 be filled, with successive collection containers Contain boxes 12 with different printed images.
- a loading device 1 is not on two magazines 4, 5 limited. You can also have three or more magazines be provided, the magazines cardboard blanks different print images included. Or at least two magazines contain the same print image if this Print image to a larger extent is desired.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Supplying Of Containers To The Packaging Station (AREA)
- Making Paper Articles (AREA)
Description
- Figur 1
- in einer Seitenansicht eine Beschickungsvorrichtung für Kartons mit zwei starr miteinander verbundenen, verschiebbaren Magazinen, wobei jedes Magazin Kartonzuschnitte mit einem bestimmten Druckbild enthält, mit einer Kugelrollbuchse als Lager und einem pneumatischen Zylinder als Antrieb, sowie mit einem Saugnapf an einem Hebel als greifendes Mittel zum Abziehen einzelner Kartonzuschnitte;
- Figur 2
- in einer Seitenansicht die Beschickungsvorrichtung der Figur 1, jedoch mit verschobenen Magazinen, sowie
- Figur 3
- in einer Seitenansicht aus einer um 90° versetzten Richtung die Beschickungsvorrichtung der Figuren 1 und 2 mit zusätzlich einem Förderband, einer darüber angeordneten Beleimungseinrichtung, sowie anschließend daran einem Faltarm und eine für die Aufnahme des Faltarms ausgebildete Faltform.
Claims (12)
- Beschickungsvorrichtung für Kartons mit mindestens zwei Magazinen (2, 3), die gleichartige Kartonzuschnitte (4, 5) enthalten und mit einem sich auf ein Magazin (2, 3) zu und von diesem weg bewegendem, greifenden Mittel (6), welches jeweils einen Kartonzuschnitt (4, 5) greift und in Richtung einer den Kartonzuschnitt (4, 5) formenden Schachtelformvorrichtung (13) abgibt, wobei die Magazine (2, 3) derart ortsveränderbar sind, so daß jedes einzelne Magazin (2, 3) wahlweise an das die Kartonzuschnitte (4, 5) greifende Mittel (6) herangeführt wird, dadurch gekennzeichnet, daß die Magazine (2, 3) starr miteinander verbunden sind, daß die Magazine 2, 3) entlang einer geraden Strecke (14) verschoben werden, daß die Strecke (14) senkrecht zur Bewegungsrichtung des die Kartonzuschnitte (2, 3) greifenden Mittels (6) verläuft, und daß die Kartonzuschnitte (4, 5) je eines Magazins (2, 3) die gleiche Bedruckung aufweisen, und in den Magazinen (2, 3) Kartonzuschnitte (4, 5) unterschiedlicher Bedruckung vorgesehen sind.
- Beschickungsvorrichtung nach Anspruch 1, dadurch gekennzeichnet, daß die Magazine (2, 3) auf mindestens einer Kugelrollbuchse (16) gelagert sind.
- Beschickungsvorrichtung nach Anspruch 1 oder Anspruch 2, dadurch gekennzeichnet, daß die Magazine (2, 3) mittels eines pneumatischen Zylinders (18) angetrieben werden.
- Beschickungsvorrichtung nach Anspruch 1 oder Anspruch 2, dadurch gekennzeichnet, daß an dem die Kartonzuschnitte (4, 5) greifenden Mittel (6) mindestens ein Saugnapf (19) vorgesehen ist.
- Beschickungsvorrichtung nach Anspruch 4, dadurch gekennzeichnet, daß der Saugnapf (19) mit einer Vakuumquelle (21) verbunden ist, und daß Mittel zur Zuschaltung und Abschaltung des Saugnapfes (19) von der Vakuumquelle (21) vorgesehen sind.
- Beschickungsvorrichtung nach Anspruch 4, dadurch gekennzeichnet, daß der Saugnapf (19) mit einer Druckluftquelle (23) verbunden ist, und daß Mittel zur Zuschaltung und Abschaltung des Saugnapfes (19) von der Druckluftquelle (23) vorgesehen sind.
- Beschickungsvorrichtung nach Anspruch 1, dadurch gekennzeichnet, daß das greifende Mittel (6) ein Saugnapf (19) ist, der taktweise bei jedem Greifvorgang zuerst mit einer Vakuumquelle (21) und dann mit einer Druckluftquelle (23) verbunden wird.
- Verfahren zum Betreiben einer Beschickungsvorrichtung für Kartons mit mindestens zwei Magazinen zur Aufnahme von Kartonzuschnitten und mit einem sich auf ein Magazin zu und von diesem weg bewegendem Mittel, welches jeweils einen Kartonzuschnitt greift und in Richtung einer den Kartonzuschnitt formenden Schachtelformvorrichtung (13) abgibt, und Magazine (2, 3) abwechselnd an das die Kartonzuschnitte (4, 5) greifende Mittel (6) geschoben werden, dadurch gekennzeichnet, daß die Magazine 2, 3) entlang einer geraden Strecke (14) verschoben werden, daß die Strecke (14) senkrecht zur Bewegungsrichtung des die Kartonzuschnitte (2, 3) greifenden Mittels (6) verläuft daß die Magazine (2,3) mit Kartonzuschnitten (4, 5) unterschiedlicher Bedruckung befüllt werden, und daß entweder die Magazine (2, 3) direkt nach jeweils einer erfolgten Entnahme eines Kartonzuschnitts (4, 5) verschoben werden oder die Magazine (2, 3) nach jeweils erfolgter Entnahme einer fest vorgegebenen Anzahl an Kartonzuschnitten (4, 5) verschoben werden.
- Verfahren nach Anspruch 8, dadurch gekennzeichnet, daß die Anzahl der Anzahl an Kartons pro Kartonreihe in einem Sammelbehälter entspricht.
- Verfahren nach Anspruch 8, dadurch gekennzeichnet, daß die Anzahl der Anzahl an Kartons in einem Sammelbehälter entspricht.
- Verfahren nach Anspruch 8, dadurch gekennzeichnet, daß das greifende Mittel (6) die Kartonzuschnitte (4) in Richtung eines Faltarmes (11) einer Schachtelformvorrichtung (13) weitergibt, daß dann die Kartonzuschnitte (5) an einer Beleimungsvorrichtung (8) beleimt werden, und daß schließlich die Kartonzuschnitte (4) durch den Faltarm (11) einzeln und taktweise in einer Faltform (10) gefaltet und bezüglich der Verleimung gepreßt werden.
- Verfahren nach Anspruch 8, dadurch gekennzeichnet, daß das greifende Mittel die Kartonzuschnitte in Richtung eines Kartonaufrichters weitergibt.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE4447098 | 1994-12-29 | ||
| DE4447098A DE4447098A1 (de) | 1994-12-29 | 1994-12-29 | Beschickungsvorrichtung für Kartons und Verfahren zum Betreiben einer Beschickungsvorrichtung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0719706A1 EP0719706A1 (de) | 1996-07-03 |
| EP0719706B1 true EP0719706B1 (de) | 1998-11-25 |
Family
ID=6537421
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95115012A Expired - Lifetime EP0719706B1 (de) | 1994-12-29 | 1995-09-23 | Beschickungsvorrichtung für Kartons und Verfahren zum Betreiben einer Beschickungsvorrichtung |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0719706B1 (de) |
| DE (2) | DE4447098A1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| IT202300018141A1 (it) * | 2023-09-04 | 2025-03-04 | Gruppo Tecnoferrari Spa | Apparato di presa e spostamento di cartoni fustellati per macchina confezionatrice |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6374581B1 (en) | 1997-09-19 | 2002-04-23 | The Mead Corporation | Feeder mechanism and hopper for two different types of cartons |
| GB9719951D0 (en) * | 1997-09-19 | 1997-11-19 | Mead Corp | Feeder mechanism and hopper |
| WO2000064746A1 (en) * | 1999-04-23 | 2000-11-02 | Tetra Laval Holdings & Finance, S.A. | Multi-product packaging machine and method with bar code reader |
| US6840176B1 (en) * | 2003-12-02 | 2005-01-11 | Creo Il. Ltd. | CTP systems having at least one multi-cassette unit and methods for loading plates |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1201743B (de) * | 1959-02-05 | 1965-09-23 | Container Corp | Vorrichtung zur Entnahme und Zufuehrung von Kartonzuschnitten in einer Maschine zum Verpacken von Dosengruppen in Wickelkartons |
| DE1901300A1 (de) * | 1969-01-11 | 1970-09-03 | Schick Dipl Ing Guenther | Stapelwechselvorrichtung zum Einlegen und zum Zufuehren von Zuschnitten aus plattenfoermigem Material,Papier,Pappe oder Folien in eine Verarbeitungsmaschine |
-
1994
- 1994-12-29 DE DE4447098A patent/DE4447098A1/de not_active Withdrawn
-
1995
- 1995-09-23 DE DE59504332T patent/DE59504332D1/de not_active Expired - Fee Related
- 1995-09-23 EP EP95115012A patent/EP0719706B1/de not_active Expired - Lifetime
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| IT202300018141A1 (it) * | 2023-09-04 | 2025-03-04 | Gruppo Tecnoferrari Spa | Apparato di presa e spostamento di cartoni fustellati per macchina confezionatrice |
Also Published As
| Publication number | Publication date |
|---|---|
| DE4447098A1 (de) | 1996-07-04 |
| DE59504332D1 (de) | 1999-01-07 |
| EP0719706A1 (de) | 1996-07-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE60303240T2 (de) | Verfahren und Vorrichtung zum Verpacken eines Produkts unter Verwendung einer flachen rohrförmigen Verpackung | |
| DE3429761C2 (de) | ||
| DE3516651A1 (de) | Verfahren und vorrichtung zur behandlung quetschbarer, tubenfoermiger behaelter und zu deren verpacken in schachteln | |
| DE69200610T2 (de) | Verfahren und Vorrichtung zum Vorbereiten von Verpackungszuschnitten. | |
| DE69916549T2 (de) | Verfahren und Maschine zum Verpacken eines Gegenstands | |
| DE69104553T2 (de) | Vorrichtung zum Herstellen von Kartons aus flachen hülsenartigen Zuschnitten. | |
| EP3010809A1 (de) | Verpackungsmaschine zum herstellen von gebinden | |
| EP0764584A2 (de) | Vorrichtung zur Verpackung | |
| EP0265870B1 (de) | Rotierender Anleger für Zuschnitte | |
| DE4447098A1 (de) | Beschickungsvorrichtung für Kartons und Verfahren zum Betreiben einer Beschickungsvorrichtung | |
| EP3027518A1 (de) | Vorrichtung zum transportieren und einsetzen von trennelementen in verpackungseinheiten | |
| WO1994026480A1 (de) | Vorrichtung, klemmwerkzeug und verfahren zum ausbrechen von zuschnittabfällen beim stanzen von karton | |
| DE102017208856A1 (de) | Transportvorrichtung und Verfahren zum Transport von Umverpackungen | |
| EP0716637B1 (de) | Verfahren und vorrichtung zum formen und etikettieren von verpackungsbehältern | |
| EP1129967B1 (de) | Greifersystem zur automatischen Entnahme von Stangen flacher Güter aus einer Transportverpackung | |
| DE2458446A1 (de) | Vorrichtung und verfahren zum einzeltransport von bogen, insbesondere zum geschwindigkeitsveraenderlichen transport von kartonzuschnitten | |
| EP3458366B1 (de) | Verfahren und vorrichtung zum etikettieren von ersten verpackungen | |
| DE4133404A1 (de) | Vorrichtung zum foerdern von aufklebern | |
| EP1112211A1 (de) | Verfahren und Vorrichtung zum Etikettieren oder Bedrucken von ineinander stapelbaren Behältern | |
| EP1475306B1 (de) | Maschine zur Herstellung von Zigarettenpackungen | |
| EP0220377A2 (de) | Verfahren und Vorrichtung zur Herstellung von etikettierten Kunststoffformlingen | |
| EP0879761A1 (de) | Verfahren und Vorrichtung zum Handhaben von Zuschnitten | |
| DE3417154A1 (de) | Maschine zum verpacken von massenartikeln | |
| DE69919477T2 (de) | Verfahren und Maschine zum Verpacken einer Gruppe von Gegenständen | |
| DE4447099A1 (de) | Vorrichtung und Verfahren zur Erzeugung von Faltschachteln aus Faltschachtelzuschnitten |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19951009 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE GB IT NL |
|
| 17Q | First examination report despatched |
Effective date: 19970827 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE GB IT NL |
|
| REF | Corresponds to: |
Ref document number: 59504332 Country of ref document: DE Date of ref document: 19990107 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19990208 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20040909 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20040913 Year of fee payment: 10 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050923 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050923 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20051124 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060401 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20050923 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20060401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070403 |