EP0337107B1 - Spinnrotor - Google Patents
Spinnrotor Download PDFInfo
- Publication number
- EP0337107B1 EP0337107B1 EP89104021A EP89104021A EP0337107B1 EP 0337107 B1 EP0337107 B1 EP 0337107B1 EP 89104021 A EP89104021 A EP 89104021A EP 89104021 A EP89104021 A EP 89104021A EP 0337107 B1 EP0337107 B1 EP 0337107B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- layer
- boron
- nickel coating
- alpha
- iron
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000009987 spinning Methods 0.000 title claims description 17
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims description 36
- 239000010410 layer Substances 0.000 claims description 30
- 238000000576 coating method Methods 0.000 claims description 23
- 239000011248 coating agent Substances 0.000 claims description 22
- JZQOJFLIJNRDHK-CMDGGOBGSA-N alpha-irone Chemical compound CC1CC=C(C)C(\C=C\C(C)=O)C1(C)C JZQOJFLIJNRDHK-CMDGGOBGSA-N 0.000 claims description 19
- 229910052759 nickel Inorganic materials 0.000 claims description 18
- 229910000859 α-Fe Inorganic materials 0.000 claims description 17
- 239000000463 material Substances 0.000 claims description 16
- OKKJLVBELUTLKV-UHFFFAOYSA-N Methanol Chemical compound OC OKKJLVBELUTLKV-UHFFFAOYSA-N 0.000 claims description 12
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 claims description 10
- 229910052796 boron Inorganic materials 0.000 claims description 9
- 238000004519 manufacturing process Methods 0.000 claims description 9
- 229910003460 diamond Inorganic materials 0.000 claims description 6
- 239000010432 diamond Substances 0.000 claims description 6
- 238000000034 method Methods 0.000 claims description 6
- 239000002344 surface layer Substances 0.000 claims description 6
- 229910052757 nitrogen Inorganic materials 0.000 claims description 5
- 229910000831 Steel Inorganic materials 0.000 claims description 4
- 239000010959 steel Substances 0.000 claims description 4
- 238000010438 heat treatment Methods 0.000 claims description 2
- 238000007383 open-end spinning Methods 0.000 claims description 2
- 239000000843 powder Substances 0.000 claims description 2
- ZOXJGFHDIHLPTG-UHFFFAOYSA-N Boron Chemical compound [B] ZOXJGFHDIHLPTG-UHFFFAOYSA-N 0.000 claims 8
- XKRFYHLGVUSROY-UHFFFAOYSA-N Argon Chemical compound [Ar] XKRFYHLGVUSROY-UHFFFAOYSA-N 0.000 claims 2
- 238000000137 annealing Methods 0.000 claims 1
- 229910052786 argon Inorganic materials 0.000 claims 1
- 239000003795 chemical substances by application Substances 0.000 claims 1
- 239000007789 gas Substances 0.000 claims 1
- 239000000203 mixture Substances 0.000 claims 1
- 230000001681 protective effect Effects 0.000 claims 1
- 238000010791 quenching Methods 0.000 claims 1
- 230000000171 quenching effect Effects 0.000 claims 1
- 239000000835 fiber Substances 0.000 description 4
- 229910000915 Free machining steel Inorganic materials 0.000 description 3
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 2
- 238000005422 blasting Methods 0.000 description 2
- -1 Boron carbides Chemical class 0.000 description 1
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 1
- 230000001464 adherent effect Effects 0.000 description 1
- 239000002318 adhesion promoter Substances 0.000 description 1
- 239000011324 bead Substances 0.000 description 1
- ZDVYABSQRRRIOJ-UHFFFAOYSA-N boron;iron Chemical compound [Fe]#B ZDVYABSQRRRIOJ-UHFFFAOYSA-N 0.000 description 1
- 229910052799 carbon Inorganic materials 0.000 description 1
- 238000005336 cracking Methods 0.000 description 1
- 239000011521 glass Substances 0.000 description 1
- 229910052742 iron Inorganic materials 0.000 description 1
- 230000007774 longterm Effects 0.000 description 1
- 239000003921 oil Substances 0.000 description 1
- 238000005457 optimization Methods 0.000 description 1
- 229910010271 silicon carbide Inorganic materials 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C8/00—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals
- C23C8/80—After-treatment
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H4/00—Open-end spinning machines or arrangements for imparting twist to independently moving fibres separated from slivers; Piecing arrangements therefor; Covering endless core threads with fibres by open-end spinning techniques
- D01H4/04—Open-end spinning machines or arrangements for imparting twist to independently moving fibres separated from slivers; Piecing arrangements therefor; Covering endless core threads with fibres by open-end spinning techniques imparting twist by contact of fibres with a running surface
- D01H4/08—Rotor spinning, i.e. the running surface being provided by a rotor
- D01H4/10—Rotors
Definitions
- the invention relates to a spinning rotor made of steel for an open-end spinning machine, in which at least the surfaces of the rotor plate which come into contact with the fibers and the thread have a borated surface layer and a nickel coating applied thereon, and a method for producing such a spinning rotor .
- the inner, bell-shaped part which comes into contact with the thread has a borated surface layer which has a nickel coating with embedded hard material grains, preferably diamond.
- a coating of the rotor improves wear resistance and delivers particularly good spinning results.
- the invention has for its object to propose a generic rotor with high wear resistance and long-term good spinning results and a method for its manufacture.
- the thin layer of alpha iron advantageously protects the borated surface layer from cracking during hardening. Since the alpha-iron layer is softer than the layers adjacent to it, it is able to absorb stress fluctuations that can develop between these two layers due to different thermal expansion, so that neither damage to the borated layer of the rotor nor to the applied nickel coating can take place due to stress cracks.
- the alpha-iron layer for example, is also able to cover microcracks in the borated surface.
- the thickness of the alpha-iron layer is only a few ⁇ m, specifically in a range from 0.5 to 8 ⁇ m, preferably from 2 to 4 ⁇ m. Such a layer thickness makes up only a small proportion of the boride layer and can be produced without an additional processing step during hardening.
- alpha-iron layer Another advantage of the alpha-iron layer is its property as an adhesion promoter between the borated surface and the nickel coating. Different properties of the base body and the applied nickel coating, for example different behavior under the influence of heat, are optimally balanced by the alpha-iron layer.
- the nickel coating in turn, proves to be a particularly suitable layer for the storage of hard material grains, for example diamond grains.
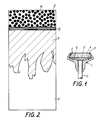
- Fig. 1 shows a spinning rotor according to the invention in section.
- Fig. 2 shows a section of the coated surface of the spinning rotor.
- the rotor plate 3 has on its inside a conical fiber collecting surface 4 which ends at a fiber collecting channel 5. A further part 6 of the inner rotor plate extends from the fiber collecting trough 5 to the end of the shaft 2.
- the inside of the rotor plate 3 consists of the borated surface layer to which a nickel coating with hard material grains 7 embedded therein has been applied.
- Fig. 2 which shows an enlarged section of the inner surface of the rotor plate, illustrates the structure of the individual layers of the inner surface of the rotor plate.
- the base material 8 is a tempered free-cutting steel. As a result of boriding, a somewhat coarser crystallized layer of Fe2B is formed, which is well interlocked with the base material.
- the layer thickness is approximately 25 to 75 ⁇ m.
- This layer is followed by the alpha-iron layer 10 according to the invention, which arises on the basis of the coating associated with the boronization process. It has a layer thickness of preferably 2 to 4 ⁇ m and is very fine crystalline.
- a nickel coating 11 with embedded hard material grains 7 takes place on this alpha iron layer 10.
- the nickel coating with the embedded hard material grains has an approximate thickness of 25 ⁇ m.
- Boron carbides, silicon carbides or diamond are suitable as hard materials.
- the size of the hard material grains is between 1 to 6 ⁇ m, but preferably in the range from 1 to 3 ⁇ m.
- the rotor formed from tempered free-cutting steel is borated in a known manner, as is described in DE-OS 33 39 852.
- the carbon content of the free cutting steel is approximately 0.4 to 0.48%.
- the rotors are tempered, that is hardened and tempered.
- the furnace atmosphere is adjusted so that the iron-boron compound is converted into a layer of preferably 2 to 4 ⁇ m.
- the furnace atmosphere consists of a high proportion of nitrogen and a small proportion of methanol.
- the furnace atmosphere was designed so that the ratio of methanol to nitrogen was 1: 2.18 x 10³ liters per hour.
- the CO content in the furnace atmosphere was approximately 14.4%, the nitrogen content approximately 56.7%.
- the hardening temperature was about 820 degrees with a holding time of 10 minutes. This converts Fe2B to Fe2 and alpha-crystalline iron.
- a nickel coating with embedded diamond powder as hard material grains was applied to the resulting alpha-iron layer.
- the applied layer thickness was approximately 25 ⁇ m.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Textile Engineering (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Spinning Or Twisting Of Yarns (AREA)
- Chemically Coating (AREA)
- Electroplating Methods And Accessories (AREA)
Description
- Die Erfindung betrifft einen Spinnrotor aus Stahl für eine Offenend-Spinnmaschine, bei dem zumindest die Flächen des Rotortellers, die mit den Fasern und dem Faden in Berührung kommen, eine borierte Oberflächenschicht und eine darauf aufgebrachte Nickelbeschichtung aufweisen, sowie ein Verfahren zur Herstellung eines solchen Spinnrotors.
- Aus der DE-OS 33 39 852 ist ein Spinnrotor bekannt, dessen innerer, glockenförmiger Teil, der mit dem Faden in Berührung kommt, eine borierte Oberflächenschicht aufweist, die eine Nickelbeschichtung mit eingebetteten Hartstoffkörnern, vorzugsweise Diamant, aufweist. Eine solche Beschichtung des Rotors verbessert den Verschleißwiderstand und liefert besonders gute Spinnergebnisse.
- Es hat sich aber gezeigt, daß manchmal Mikrorisse in den Beschichtungen auftreten, die die Qualität des Rotors und damit des Spinnergebnisses beinträchtigen können.
- Der Erfindung liegt die Aufgabe zugrunde, einen gattungsgemäßen Rotor mit hohem Verschleißwiderstand und langzeitig guten Spinnergebnissen und ein Verfahren zu seiner Herstellung vorzuschlagen.
- Die Lösung dieser Aufgabe erfolgt erfindungsgemäß mit Hilfe der kennzeichnenden Merkmale der Ansprüche 1 und 6.
- Die dünne Schicht aus Alpha-Eisen schützt die borierte Oberflächenschicht während des Härtens vorteilhaft vor Rißbildung. Da die Alpha-Eisen-Schicht weicher ist als die ihr benachbarten Schichten, ist sie in der Lage, Spannungsschwankungen, die sich zwischen diesen beiden Schichten aufgrund unterschiedlicher Wäremeausdehnung ausbilden können, aufzufangen, so daß weder eine Beschädigung der borierten Schicht des Rotors, noch der aufgetragenen Nickelbeschichtung infolge von Spannungsrissen erfolgen kann. Die Alpha-Eisen-Schicht ist beispielsweise auch in der Lage, Mikrorisse in der borierten Oberfläche abzudecken.
- In Weiterbildung der Erfindung hat sich als vorteilhaft erwiesen, wenn die Dicke der Alpha-Eisen-Schicht nur wenige µm beträgt, und zwar in einem Bereich von 0,5 bis 8 µm, vorzugsweise von 2 bis 4 µm. Eine solche Schichtdicke macht nur einen geringen Anteil der Boridschicht aus und läßt sich ohne einen zusätzlichen Verarbeitungsschritt während des Härtens erzeugen.
- Ein weiterer Vorteil der Alpha-Eisen-Schicht besteht in ihrer Eigenschaft als Haftvermittler zwischen der borierten Oberfläche und der Nickelbeschichtung. Unterschiedliche Eigenschaften des Grundkörpers und der aufgebrachten Nickelbeschichtung, beispielsweise unterschiedliches Verhalten unter Wärmeeinfluß, werden durch die Alpha-Eisen-Schicht optimal ausgeglichen.
- Die Nickelbeschichtung wiederum erweist sich als besonders geeignete Schicht für die Einlagerung von Hartstoffkörnern, beispielsweise Diamantkörnern.
- Anhand von einem Ausführungsbeispiel wird der erfindungsgemäße Rotor sowie sein Herstellungsverfahren näher erläutert.
- Fig. 1 zeigt einen erfindungsgemäßen Spinnrotor im Schnitt.
- Fig. 2 zeigt einen Ausschnitt aus der beschichteten Oberfläche des Spinnrotors.
- Der Spinnrotor 1 nach Fig. 1 besteht aus Stahl und ist auf eine Welle 2 aufgepreßt. Der Rotorteller 3 weist auf seiner Innenseite eine kegelig ausgebildete Fasersammelfläche 4 auf, die an einer Fasersammelrinne 5 endet. Von der Fasersammelrinne 5 aus erstreckt sich ein weiterer Teil 6 des inneren Rotortellers bis zum Ende der Welle 2.
- Das Innere des Rotortellers 3 besteht aus der borierten Oberflächenschicht, auf die eine Nickelbeschichtung mit darin eingebetteten Hartstoffkörnern 7 aufgebracht worden ist.
Fig. 2, die einen vergrößerten Ausschnitt aus der Innenfläche des Rotortellers zeigt, verdeutlicht den Aufbau der einzelnen Schichten der Innenfläche des Rotortellers. - Der Basiswerkstoff 8 ist ein vergüteter Automatenstahl. Infolge des Borierens bildet sich eine etwas gröber kristallisierte borierte Schicht aus Fe₂B, die gut mit dem Basiswerkstoff verzahnt ist. Die Schichtdicke beträgt etwa 25 bis 75 µm.
- An diese Schicht schließt sich die erfindungsgemäße Alpha-Eisen-Schicht 10 an, die aufgrund der dem Borierungsprozeß angeschlossenen Vergütung entsteht. Sie weist eine Schichtdicke von vorzugsweise 2 bis 4 µm auf und ist sehr feinkristallin.
- Auf diese Alpha-Eisen-Schicht 10 erfolgt eine Nickelbeschichtung 11 mit eingelagerten Hartstoffkörnern 7. Die Nickelbeschichtung mit den eingelagerten Hartstoffkörnern hat eine ungefähre Dicke von 25 µm. Als Hartstoffe sind beispielsweise Borkarbide, Siliciumkarbide oder Diamant geeignet. Die Größe der Hartstoffkörner liegt zwischen 1 bis 6 µm, vorzugsweise aber im Bereich von 1 bis 3 µm.
- Anhand eines Ausführungsbeispiels wird die Erzeugung der erfindungsgemäßen Alpha-Eisen-Schicht bei der Herstellung eines Rotors erläutert.
- Der aus vergütetem Automatenstahl geformte Rotor wird in bekannter Weise, wie es in der DE-OS 33 39 852 beschrieben ist, boriert. Der Kohlenstoffgehalt des Automatenstahls beträgt etwa 0,4 bis 0,48 %.
- Nach dem Borieren werden die Rotoren vergütet, das heißt gehärtet und angelassen. Während des Härtens wird die Ofenatmosphäre so eingestellt, daß eine Umwandlung der Eisen-Bor-Verbindung in einer Schicht von vorzugsweise 2 bis 4 µm erfolgt. Die Ofenatmosphäre setzt sich zusammen aus einem hohen Anteil von Stickstoff und einem geringen Anteil von Methanol. In einem ausgeführten Beispiel wurde die Ofenatmosphäre so zusammengestellt, daß das Verhältnis von Methanol zu Stickstoff sich wie 1 : 2,18 x 10³ Liter pro Stunde einstellte. Der CO-Anteil in der Ofenatmosphäre betrug etwa 14,4 %, der Stickstoffanteil etwa 56,7 %. Die Härtetemperatur betrug etwa 820 Grad bei 10 Minuten Haltezeit. Dabei erfolgt eine Umwandlung von Fe₂B zu Fe₂ und Alpha-kristallinem Eisen.
- Nach dem Härten erfolgte ein Abschrecken im Ölbad und darauf ein Anlassen im Vakuumofen bei etwa 380 Grad Celsius.
- Auf die so entstandene Alpha-Eisen-Schicht erfolgte der Auftrag einer Nickelbeschichtung mit eingelagertem Diamantpulver als Hartstoffkörner. Die aufgetragene Schichtdicke betrug etwa 25 µm.
- Anschließend erfolgte eine Wärmebehandlung bei etwa 350 Grad Celsius über zwei Stunden in einem Ofen zur Aushärtung der Nickelbeschichtung. Eine Endbehandlung durch Strahlen mit Glasperlen von etwa 40 bis 80 µm Durchmesser kann diese Behandlung abschließen. Das Strahlen reinigt die Oberfläche und schlägt nichthaftende Hartstoffkörner aus dieser Oberfläche heraus. Damit tragen nur fest in der Oberfläche verankerte Hartstoffkörner zur Optimierung des Spinnprozesses bei.
- Die Erzeugung einer Alpha-Eisen-Schicht auf einer borierten Oberfläche wird hier an einem konkreten Ausführungsbeispiel erläutert. Sie braucht aber nicht auf die Herstellung von Spinnrotoren beschränkt zu sein, sondern denkbar ist ein solches Verfahren bei allen borierten Oberflächen, die mit einer Nickelbeschichtung versehen werden sollen. Dabei ist es nicht erforderlich, daß beispielsweise Hartstoffkörner in die Oberfläche eingelagert werden.
Claims (8)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3810775 | 1988-03-30 | ||
| DE3810775A DE3810775C2 (de) | 1988-03-30 | 1988-03-30 | Spinnrotor |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0337107A1 EP0337107A1 (de) | 1989-10-18 |
| EP0337107B1 true EP0337107B1 (de) | 1992-06-17 |
Family
ID=6351044
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89104021A Expired - Lifetime EP0337107B1 (de) | 1988-03-30 | 1989-03-07 | Spinnrotor |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US4928477A (de) |
| EP (1) | EP0337107B1 (de) |
| JP (1) | JP2716513B2 (de) |
| DE (2) | DE3810775C2 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015114731A1 (de) | 2015-09-03 | 2017-03-09 | Maschinenfabrik Rieter Ag | Offenend-Spinnrotor mit einer Rotortasse aus vergütbarem Stahlmaterial |
Families Citing this family (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3927910A1 (de) * | 1989-08-24 | 1991-02-28 | Stahlecker Fritz | Falschdrallduese fuer pneumatisches falschdrallspinnen |
| US5721055A (en) * | 1995-01-03 | 1998-02-24 | Surface Technology, Inc. | Lubricated textile spinning machinery parts |
| DE19713359B4 (de) * | 1997-03-29 | 2005-12-08 | Saurer Gmbh & Co. Kg | Spinnrotor für eine Offenend-Spinnmaschine und Verfahren zu seiner Beschichtung |
| DE19822265B4 (de) * | 1997-06-13 | 2006-07-06 | Rieter Ingolstadt Spinnereimaschinenbau Ag | Offenend-Spinnrotor und Verfahren zu seiner Herstellung |
| DE19743597A1 (de) * | 1997-10-02 | 1999-04-08 | Fritz Stahlecker | OE-Spinnrotor |
| CA2281142C (en) | 1999-08-30 | 2008-11-18 | Stephen Jefferies | Rock guard for a trailer |
| CA2282771A1 (en) | 1999-09-17 | 2001-03-17 | Dale William Mackenzie | Method and apparatus for boronizing a metal workpiece |
| DE19947547A1 (de) * | 1999-10-02 | 2001-04-05 | Schlafhorst & Co W | Spinnrotor für eine Offenend-Spinnmaschine |
| DE102007036927A1 (de) * | 2007-08-04 | 2009-02-12 | Oerlikon Textile Gmbh & Co. Kg | Spinnmittel einer Textilmaschine |
| DE102008000201A1 (de) | 2008-01-31 | 2009-08-06 | Rieter Ingolstadt Gmbh | Spinnrotor für eine Offenend-Spinnvorrichtung |
| DE102015103229A1 (de) * | 2015-03-05 | 2016-09-08 | Maschinenfabrik Rieter Ag | Rotorteller, Spinnrotor sowie Verfahren zur Herstellung eines Rotortellers eines Spinnrotors |
| DE102017113029A1 (de) | 2017-06-13 | 2018-12-13 | Maschinenfabrik Rieter Ag | Verfahren zur Herstellung einer Rotortasse für einen Offenend-Spinnrotor sowie Rotortasse für einen Offenend-Spinnrotor |
| CN221320205U (zh) * | 2023-09-28 | 2024-07-12 | 乐擎智能科技(苏州)有限公司 | 一种纺纱用转杯 |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2110271A3 (en) * | 1970-10-07 | 1972-06-02 | Sybron Corp | Coating metal - with metal and insoluble inert material in non-electrolytic bath |
| DE2909739A1 (de) * | 1979-03-13 | 1980-09-18 | Stahlecker Fritz | Spinnrotor fuer eine offenend- spinnvorrichtung |
| CH643597A5 (de) * | 1979-12-20 | 1984-06-15 | Maag Zahnraeder & Maschinen Ag | Verfahren zum regelbaren aufkohlen oder erwaermen in schutzgas von werkstuecken aus stahl. |
| DE3016675C2 (de) * | 1980-04-30 | 1986-06-12 | W. Schlafhorst & Co, 4050 Mönchengladbach | Offenend-Spinnvorrichtung |
| GB2104111B (en) * | 1981-08-14 | 1986-04-23 | Reiners Verwaltungs Gmbh | Spinning rotor for an open-end spinning machine and method for its production |
| DE3144384A1 (de) * | 1981-11-07 | 1983-05-19 | W. Schlafhorst & Co, 4050 Mönchengladbach | Spinnrotor fuer eine offenend-spinnmaschine und verfahren zu seiner herstellung |
| DE3322957C2 (de) * | 1983-06-25 | 1985-05-15 | Hauni-Werke Körber & Co KG, 2050 Hamburg | Verfahren zum Härten der Oberfläche von Gegenständen aus Eisenwerkstoff |
| DE3339852A1 (de) * | 1983-11-04 | 1985-05-15 | W. Schlafhorst & Co, 4050 Mönchengladbach | Spinnrotor |
| JPS60197880A (ja) * | 1984-03-19 | 1985-10-07 | Aisin Seiki Co Ltd | 複合メッキ被膜 |
| DE3429511A1 (de) * | 1984-08-10 | 1986-02-20 | W. Schlafhorst & Co, 4050 Mönchengladbach | Spinnrotor fuer eine oe-spinnmaschine und verfahren zum herstellen des spinnrotors |
| JPS63295720A (ja) * | 1987-05-21 | 1988-12-02 | Kanai Hiroyuki | 紡機用リング |
-
1988
- 1988-03-30 DE DE3810775A patent/DE3810775C2/de not_active Expired - Fee Related
-
1989
- 1989-03-07 EP EP89104021A patent/EP0337107B1/de not_active Expired - Lifetime
- 1989-03-07 DE DE8989104021T patent/DE58901660D1/de not_active Expired - Lifetime
- 1989-03-30 JP JP1076880A patent/JP2716513B2/ja not_active Expired - Lifetime
- 1989-03-30 US US07/331,638 patent/US4928477A/en not_active Expired - Lifetime
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015114731A1 (de) | 2015-09-03 | 2017-03-09 | Maschinenfabrik Rieter Ag | Offenend-Spinnrotor mit einer Rotortasse aus vergütbarem Stahlmaterial |
Also Published As
| Publication number | Publication date |
|---|---|
| DE3810775C2 (de) | 1996-05-23 |
| US4928477A (en) | 1990-05-29 |
| JP2716513B2 (ja) | 1998-02-18 |
| JPH026631A (ja) | 1990-01-10 |
| EP0337107A1 (de) | 1989-10-18 |
| DE3810775A1 (de) | 1989-10-12 |
| DE58901660D1 (de) | 1992-07-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3810775C2 (de) | Spinnrotor | |
| DE69119690T2 (de) | Presswalze für Papiermaschinen | |
| EP2668309B1 (de) | Gleitelement, insbesondere kolbenring, mit einer beschichtung sowie verfahren zur herstellung eines gleitelements | |
| DE2525185C3 (de) | Hartmetallkörper | |
| DE102011002730B4 (de) | Verfahren zum Herstellen einer korrosionsbeständigen Feder, sowie danach hergestellte korrosionsbeständige Feder | |
| DE3545826A1 (de) | Kolbenring | |
| CH674211A5 (de) | ||
| DE3118123A1 (de) | "mit faser verstaerktes glas" | |
| DE102004052673A1 (de) | Verschleißarme Bremsscheibe oder Bremstrommel und Verfahren zu deren Herstellung | |
| CH697753A2 (de) | Beschichteter Ringläufer mit Nanopartikeln. | |
| DE2211991B2 (de) | Kammdraht für Kratzengarnitur | |
| EP0201602B1 (de) | Ring für spinnmaschinen | |
| EP0798402B1 (de) | Oxidationsschutzschicht | |
| DE102012007815A1 (de) | Sägedraht und Verfahren zu dessen Herstellung | |
| DE3880862T2 (de) | Durch galvanische abscheidung hergestellte schleifscheibe. | |
| DE3501823A1 (de) | Verschleissbestaendiger kolbenring | |
| EP1598456B1 (de) | Ringläufer und Verfahren zu dessen Herstellung | |
| DE102019209420A1 (de) | Reibbremskörper für eine Reibbremse, Reibbremse und Verfahren zur Herstellung eines Reibbremskörpers | |
| EP0448510A1 (de) | Verfahren zur Vermeidung von Rissen in Trenn- und Schleifscheiben | |
| EP0406686A2 (de) | Verschleiss-Scheiben für Kräuselmaschinen | |
| WO2001083864A1 (de) | Ringläufer und verfahren zu dessen herstellung | |
| DE69807155T2 (de) | Verfahren zur Herstellung einer Stahlfeder, Stahlfeder und Stahl zur Herstellung der Stahlfeder | |
| DE3535148C2 (de) | ||
| DE2909739A1 (de) | Spinnrotor fuer eine offenend- spinnvorrichtung | |
| DE1166230B (de) | Verfahren zur Herstellung von Lagerteilen in Form von spitzigen Zapfen und Wellen aus nichtrostendem und hoechstens schwach magnetischem Drahtmaterial |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): CH DE FR IT LI |
|
| 17P | Request for examination filed |
Effective date: 19900312 |
|
| 17Q | First examination report despatched |
Effective date: 19910913 |
|
| ITF | It: translation for a ep patent filed | ||
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: W. SCHLAFHORST AG & CO. |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE FR IT LI |
|
| REF | Corresponds to: |
Ref document number: 58901660 Country of ref document: DE Date of ref document: 19920723 |
|
| ET | Fr: translation filed | ||
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| 26 | Opposition filed |
Opponent name: RIETER INGOLSTADT SPINNEREIMASCHINENBAU AG Effective date: 19930317 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19990317 Year of fee payment: 11 |
|
| APAC | Appeal dossier modified |
Free format text: ORIGINAL CODE: EPIDOS NOAPO |
|
| PLBN | Opposition rejected |
Free format text: ORIGINAL CODE: 0009273 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION REJECTED |
|
| 27O | Opposition rejected |
Effective date: 19990420 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20001130 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| APAH | Appeal reference modified |
Free format text: ORIGINAL CODE: EPIDOSCREFNO |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20060406 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20070326 Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20070618 Year of fee payment: 19 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070331 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080307 |