CN112222746A - A kind of pipe automatic welding equipment - Google Patents
A kind of pipe automatic welding equipment Download PDFInfo
- Publication number
- CN112222746A CN112222746A CN202011067226.5A CN202011067226A CN112222746A CN 112222746 A CN112222746 A CN 112222746A CN 202011067226 A CN202011067226 A CN 202011067226A CN 112222746 A CN112222746 A CN 112222746A
- Authority
- CN
- China
- Prior art keywords
- welded
- plate
- top surface
- wall
- jaw chuck
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K37/00—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass
- B23K37/04—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass for holding or positioning work
- B23K37/053—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass for holding or positioning work aligning cylindrical work; Clamping devices therefor
- B23K37/0533—External pipe alignment clamps
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K37/00—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass
- B23K37/02—Carriages for supporting the welding or cutting element
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K37/00—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass
- B23K37/04—Auxiliary devices or processes, not specially adapted for a procedure covered by only one of the other main groups of this subclass for holding or positioning work
- B23K37/0426—Fixtures for other work
- B23K37/0435—Clamps
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K2101/00—Articles made by soldering, welding or cutting
- B23K2101/04—Tubular or hollow articles
- B23K2101/06—Tubes
Landscapes
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Butt Welding And Welding Of Specific Article (AREA)
Abstract
The invention discloses automatic pipe welding equipment which comprises a bottom plate, wherein one side of the top surface of the bottom plate is welded with a 20866a type installation frame, the 20866two sides of the inner wall of the type installation frame are provided with first sliding grooves, the inner parts of the first sliding grooves are connected with a transverse plate in a sliding manner, the bottom of one end of the transverse plate is provided with a servo motor, the end part of an output shaft of the servo motor is fixedly provided with a first circular plate through a coupler, the bottom of the first circular plate is welded with a cylindrical block, one side of each protruding block is welded with an adjusting mechanism, the inner parts of the adjusting mechanisms are screwed with a clamping mechanism, the top surface of each upright post is welded with a supporting platform, the top surface of the supporting platform is positioned under the first three-jaw chuck, and a second three-jaw chuck is arranged, so that the invention is convenient for quickly positioning a pipeline workpiece, the, the efficiency of welding is improved, has reduced manpower resources simultaneously and the cost is reduced.
Description
Technical Field
The invention belongs to the technical field of ship manufacturing, and particularly relates to automatic pipe welding equipment.
Background
Quality is the life of the product, and welding parameters, actions and processes directly related to welding quality play a decisive role in welding quality. Therefore, it is important to improve the welding quality to control the welding operation. At present, in the field of welding, the welding of circular workpieces is difficult to accomplish stably by manpower in the ship manufacturing industry, the technical level requirement on welders is high, and the efficiency is low, so that in order to ensure the product quality of shipbuilding, the difficulty and the requirement of the process are that automatic equipment is used for replacing manual circular work welding and how to position quickly.
Traditional manual welding, it is unstable to have welding quality, and welding efficiency is low, and follow-up process that needs processing simultaneously, polishes, repair welding is more, influences whole shipbuilding cycle, increases manual work and welding cost, and it is higher to personnel's technical merit, is difficult to find numerous suitable welders.
Therefore, the automatic pipe welding equipment is provided for solving the problems in the prior art, the circular pipeline workpiece is convenient to position and adjust quickly, the welding efficiency is improved, time and labor are saved, the production and labor cost of enterprises is reduced, and the welding is more flexible.
Disclosure of Invention
The invention aims to provide automatic pipe welding equipment to solve the problems that in the prior art, pipeline workpieces are inconvenient to position and adjust quickly, welding is troublesome, welding efficiency is low, a large amount of manpower resources are wasted, enterprise cost is increased and the like.
In order to achieve the purpose, the invention adopts the following technical scheme:
an automatic pipe welding device comprises a bottom plate, wherein 20866;) type mounting frames are welded on one side of the top surface of the bottom plate, first sliding grooves are formed in two sides of the inner wall of the 20866; -type mounting frames, a transverse plate is connected to the inside of the first sliding grooves in a sliding mode, a hydraulic cylinder is installed below the transverse plate and located on the top surface of the bottom plate, the output end of the hydraulic cylinder is welded to the bottom of the transverse plate, a servo motor is installed at the bottom of one end of the transverse plate, a first circular plate is fixed to the end portion of an output shaft of the servo motor through a coupler, a cylindrical block is welded to the bottom of the first circular plate, a first bearing is connected to the end portion of the cylindrical block in an interference mode, a second circular plate is fixed to the outer wall of the first bearing, a first three-jaw chuck is installed to the bottom of the second circular plate, a protruding block is welded, the welding gun is clamped inside the clamping mechanism, the stand column is welded to the top surface of the bottom plate below the first three-jaw chuck, the supporting platform is welded to the top surface of the stand column, the second three-jaw chuck is installed under the top surface of the supporting platform, and the lifting mechanisms are symmetrically installed on the bottom of the supporting platform on the two sides of the second three-jaw chuck.
Preferably, adjustment mechanism includes the rectangular block, the rectangular block welding is in one side of lug, the second spout has been seted up to the inside of rectangular block, it has the second bearing to inlay on one side inner wall of second spout, the inside interference of second bearing is connected with first threaded rod, the tip of first threaded rod runs through second spout key connection and is connected with first carousel.
Preferably, clamping mechanism includes first slider, first slider spiro union is on the outer wall of first threaded rod, one side welding of first slider has the mounting bracket, one side of mounting bracket is seted up flutedly, it has the third bearing to inlay on the inner wall of recess, the inside interference of third bearing is connected with the second threaded rod, the spiro union has the pinch-off blades on the outer wall of second threaded rod, welder presss from both sides tightly in the inside of pinch-off blades and mounting bracket, the tip of second threaded rod runs through the notch key and is connected with the second carousel.
Preferably, the lifting mechanism comprises an air cylinder, and a rectangular support plate is welded in the output end of the air cylinder, which penetrates through the supporting platform.
Preferably, the top surface of the supporting platform is provided with a clamping groove matched with the rectangular supporting plate.
Preferably, the second sliding blocks are symmetrically welded to two sides of the end portion of the transverse plate and are connected to the inside of the first sliding groove in a sliding mode.
Preferably, the outer wall of the servo motor is welded with a connecting lug, and the connecting lug is mounted at the bottom of the transverse plate through a screw.
Preferably, an annular baffle is arranged on the outer wall of the first three-jaw chuck.
The invention has the technical effects and advantages that: compared with the prior art, the automatic pipe welding equipment provided by the invention has the following advantages:
1. the servo motor, the first three-jaw chuck and the second three-jaw chuck are used for conveniently and quickly positioning the pipeline workpiece, and then the servo motor drives the welding gun to rotate for welding, so that the pipeline work can be quickly positioned, the welding is more convenient, time and labor are saved, and the welding efficiency is improved;
2. according to the invention, through the arrangement of the adjusting mechanism and the lifting mechanism, the rectangular supporting plate can be driven to move up and down through the work of the air cylinder, so that a pipeline workpiece can be more stable during welding, then the adjusting structure can horizontally adjust the welding output end, so that pipeline workpieces with different sizes can be welded, and the welding is more convenient and flexible.
Drawings
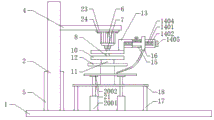
FIG. 1 is a schematic cross-sectional front view of the present invention;
FIG. 2 is a front view of the present invention;
FIG. 3 is a schematic side sectional view of the clamping mechanism of the present invention;
FIG. 4 is a top view of the cross plate of the present invention.
In the figure: 1. a base plate; 2. 20866a type mounting rack; 3. a first chute; 4. a transverse plate; 5. a hydraulic cylinder; 6. a servo motor; 7. a first circular plate; 8. a cylindrical block; 9. a first bearing; 10. a second circular plate; 11. a first three-jaw chuck; 12. an annular baffle; 13. a bump; 14. an adjustment mechanism; 1401. a rectangular block; 1402. a second chute; 1403. a second bearing; 1404. a first threaded rod; 1405. a first turntable; 15. a clamping mechanism; 1501. a first slider; 1502. a mounting frame; 1503. a groove; 1504. a third bearing; 1505. a second threaded rod; 1506. a clamping plate; 1507. a second turntable; 16. a welding gun; 17. a column; 18. a support platform; 19. a second three-jaw chuck; 20. a lifting mechanism; 2001. a cylinder; 2002. a rectangular support plate; 21. a card slot; 22. a second slider; 23. connecting lugs; 24. and (4) screws.
Detailed Description
The technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only a part of the embodiments of the present invention, and not all of the embodiments. The specific embodiments described herein are merely illustrative of the invention and do not delimit the invention. All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present invention.
The invention provides automatic pipe welding equipment as shown in figures 1-4, which comprises a bottom plate 1, wherein one side of the top surface of the bottom plate 1 is welded with a 20866a section mounting frame 2, 20866a first sliding groove 3 is formed in two sides of the inner wall of the section mounting frame 2, a transverse plate 4 is connected inside the first sliding groove 3 in a sliding manner, a hydraulic cylinder 5 is arranged below the transverse plate 4 and positioned on the top surface of the bottom plate 1, the output end of the hydraulic cylinder 5 is welded at the bottom of the transverse plate 4, a servo motor 6 is arranged at the bottom of one end of the transverse plate 4, a first circular plate 7 is fixed at the end part of an output shaft of the servo motor 6 through a coupler, a cylindrical block 8 is welded at the bottom of the first circular plate 7, a first bearing 9 is connected at the end part of the cylindrical block 8 in an interference manner, a second circular plate 10 is fixed on the outer wall of the first bearing 9, a first, an adjusting mechanism 14 is welded on one side of the protruding block 13, a clamping mechanism 15 is screwed inside the adjusting mechanism 14, a welding gun 16 is clamped inside the clamping mechanism 15, an upright post 17 is welded on the top surface of the bottom plate 1 below the first three-jaw chuck 11, a supporting platform 18 is welded on the top surface of the upright post 17, a second three-jaw chuck 19 is installed right below the first three-jaw chuck 11 on the top surface of the supporting platform 18, and lifting mechanisms 20 are symmetrically installed at the bottom of the supporting platform 18 on two sides of the second three-jaw chuck 19.
Preferably, the adjusting mechanism 14 includes a rectangular block 1401, the rectangular block 1401 is welded on one side of the protruding block 13, a second sliding slot 1402 is opened inside the rectangular block 1401, a second bearing 1403 is embedded on an inner wall of one side of the second sliding slot 1402, a first threaded rod 1404 is connected inside the second bearing 1403 in an interference manner, and an end portion of the first threaded rod 1404 penetrates through the second sliding slot 1402 and is connected with a first rotating disk 1405 in a key manner.
By adopting the technical scheme, the welding gun 16 can be conveniently adjusted back and forth, the welding gun 16 can conveniently weld pipeline workpieces of different sizes, and the use is flexible and convenient.
Preferably, the clamping mechanism 15 includes a first slider 1501, the first slider 1501 is screwed on the outer wall of a first threaded rod 1404, a mounting frame 1502 is welded on one side of the first slider 1501, a groove 1503 is formed on one side of the mounting frame 1502, a third bearing 1504 is embedded on the inner wall of the groove 1503, a second threaded rod 1505 is connected to the inside of the third bearing 1504 in an interference manner, a clamping plate 1506 is screwed on the outer wall of the second threaded rod 1505, the welding gun 16 is clamped inside the clamping plate 1506 and the mounting frame 1502, and a second rotary disc 1507 is keyed on the end of the second threaded rod 1505 through the groove 1503.
Through adopting above-mentioned technical scheme, be convenient for like this carry out the centre gripping to welding gun 16, conveniently change welding gun 16, use more nimble.
Preferably, the lifting mechanism 20 includes a cylinder 2001, and a rectangular support plate 2002 is welded to an output end of the cylinder 2001, penetrating through the inside of the support platform 18.
Through adopting above-mentioned technical scheme, can be convenient for adjust the height of steel sheet like this, make things convenient for the pipeline work piece to run through the steel sheet, the steel sheet degree steel sheet of being convenient for supports, uses the more stability of welding.
Preferably, the top surface of the supporting platform 18 is provided with a slot 21 matching with the rectangular supporting plate 2002.
By adopting the technical scheme, the rectangular support plate 2002 can be just clamped in the clamping groove 21 when being contracted, so that the support platform 18 can be ensured to be smooth, and the appearance is more attractive.
Preferably, the two sides of the end of the transverse plate 4 are symmetrically welded with second sliding blocks 22, and the second sliding blocks 22 are slidably connected inside the first sliding chute 3.
Through adopting above-mentioned technical scheme, can have fine limiting displacement to diaphragm 4 like this, can make diaphragm 4 more stable at the in-process that rises or descends moreover.
Preferably, a connecting lug 23 is welded on the outer wall of the servo motor 6, and the connecting lug 23 is installed at the bottom of the transverse plate 4 through a screw 24.
By adopting the technical scheme, the servo motor 6 can be conveniently installed, and the overhaul and the maintenance are convenient.
Preferably, an annular baffle 12 is mounted on the outer wall of the first three-jaw chuck 11.
Through adopting above-mentioned technical scheme, can have certain limit function, prevent that first three-jaw chuck 11 from stretching into pipeline work piece inside too deeply.
The working principle is as follows: when the pipeline welding fixture is used, a pipeline workpiece to be welded is clamped on the outer wall of the second three-jaw chuck 19, the second three-jaw chuck 19 works to fix the pipeline workpiece, at this time, a steel plate to be welded is sleeved on the outer wall of the pipeline workpiece, then the air cylinder 2001 works to drive the rectangular support plate 2002 positioned at the output end of the top surface of the air cylinder 2001 to extend upwards, so that the steel plate can be supported, used and welded more stably, at this time, the hydraulic cylinder 5 works to drive the transverse plate 4 to move downwards, at this time, the first three-jaw chuck 11 positioned at the end part of the transverse plate 4 is just clamped in the upper part of the pipeline workpiece, then the first three-jaw chuck 11 works to fix the pipeline workpiece again, at this time, the first rotary disc 1405 is rotated to drive the first threaded rod 1404 to rotate under the action of the second bearing 1403, at this time, the clamping mechanism 15 positioned on the outer wall of the, when reaching the crossing department stall of pipeline work piece and steel sheet, at this moment servo motor 6 work drives first plectane 7 through cylindric piece 8 and first bearing 9 and rotates, welder 16 that this moment is located on clamping mechanism 15 will follow and rotate and weld the butt joint, can fix a position fast like this in welding process, it is more convenient to weld, labour saving and time saving improves welded efficiency, and reduce the manufacturing cost of enterprise, adjustment mechanism 14 can carry out round trip's removal to welder 16 simultaneously, can weld the pipeline work piece of equidimension not like this in welding process, it is more convenient in a flexible way to use.
Finally, it should be noted that: although the present invention has been described in detail with reference to the foregoing embodiments, it will be apparent to those skilled in the art that modifications may be made to the embodiments or portions thereof without departing from the spirit and scope of the invention.
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011067226.5A CN112222746A (en) | 2020-10-05 | 2020-10-05 | A kind of pipe automatic welding equipment |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202011067226.5A CN112222746A (en) | 2020-10-05 | 2020-10-05 | A kind of pipe automatic welding equipment |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN112222746A true CN112222746A (en) | 2021-01-15 |
Family
ID=74120643
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202011067226.5A Pending CN112222746A (en) | 2020-10-05 | 2020-10-05 | A kind of pipe automatic welding equipment |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN112222746A (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113333920A (en) * | 2021-07-15 | 2021-09-03 | 景津环保股份有限公司 | Automatic rotary welding tool for round weldment of filter press and automatic electric welding equipment for gas-shielded round weld |
| CN113770495A (en) * | 2021-10-16 | 2021-12-10 | 芜湖双翼液压件有限公司 | Special-shaped steel pipe welding automation unit |
| CN115890080A (en) * | 2022-12-26 | 2023-04-04 | 东方电气集团东方锅炉股份有限公司 | A gasification furnace quenching ring adjustable welding tool and its use method |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2012121064A (en) * | 2010-12-10 | 2012-06-28 | Ihi Corp | Fixing structure, and pipe end welding device |
| CN103045965A (en) * | 2012-12-27 | 2013-04-17 | 内蒙古包钢钢联股份有限公司 | Technique for manufacturing steel plate for 600MPa hydropower steel penstock |
| CN103692099A (en) * | 2013-12-20 | 2014-04-02 | 安东石油技术(集团)有限公司 | Screen pipe welding machine and screen pipe welding method |
| CN103846595A (en) * | 2012-12-04 | 2014-06-11 | 青岛三利中德美水设备有限公司 | Welding tool for through pipe and flange of filter |
| CN108000023A (en) * | 2017-12-19 | 2018-05-08 | 安阳工学院 | The welder and its welding method of a kind of rear axle ring flange and connecting tube |
| WO2018103081A1 (en) * | 2016-12-09 | 2018-06-14 | 冯庆柱 | Laser composite welding device |
| CN209078104U (en) * | 2018-12-05 | 2019-07-09 | 宁晋县昱恒机械制造有限公司 | A kind of fitting circular seam bonding machine |
| CN213998420U (en) * | 2020-10-05 | 2021-08-20 | 福建通号信息科技有限公司 | Automatic pipe welding equipment |
-
2020
- 2020-10-05 CN CN202011067226.5A patent/CN112222746A/en active Pending
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2012121064A (en) * | 2010-12-10 | 2012-06-28 | Ihi Corp | Fixing structure, and pipe end welding device |
| CN103846595A (en) * | 2012-12-04 | 2014-06-11 | 青岛三利中德美水设备有限公司 | Welding tool for through pipe and flange of filter |
| CN103045965A (en) * | 2012-12-27 | 2013-04-17 | 内蒙古包钢钢联股份有限公司 | Technique for manufacturing steel plate for 600MPa hydropower steel penstock |
| CN103692099A (en) * | 2013-12-20 | 2014-04-02 | 安东石油技术(集团)有限公司 | Screen pipe welding machine and screen pipe welding method |
| WO2018103081A1 (en) * | 2016-12-09 | 2018-06-14 | 冯庆柱 | Laser composite welding device |
| CN108000023A (en) * | 2017-12-19 | 2018-05-08 | 安阳工学院 | The welder and its welding method of a kind of rear axle ring flange and connecting tube |
| CN209078104U (en) * | 2018-12-05 | 2019-07-09 | 宁晋县昱恒机械制造有限公司 | A kind of fitting circular seam bonding machine |
| CN213998420U (en) * | 2020-10-05 | 2021-08-20 | 福建通号信息科技有限公司 | Automatic pipe welding equipment |
Non-Patent Citations (2)
| Title |
|---|
| 刘自军;潘乾刚;: "压水堆核电站核岛主设备焊接制造工艺及窄间隙焊接技术", 电焊机, no. 02, 20 February 2010 (2010-02-20) * |
| 黄政艳;林胜;戴建树;: "一种立柱式管板自动焊机定位夹紧机构的设计", 焊接技术, no. 06, 28 June 2013 (2013-06-28) * |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113333920A (en) * | 2021-07-15 | 2021-09-03 | 景津环保股份有限公司 | Automatic rotary welding tool for round weldment of filter press and automatic electric welding equipment for gas-shielded round weld |
| CN113770495A (en) * | 2021-10-16 | 2021-12-10 | 芜湖双翼液压件有限公司 | Special-shaped steel pipe welding automation unit |
| CN115890080A (en) * | 2022-12-26 | 2023-04-04 | 东方电气集团东方锅炉股份有限公司 | A gasification furnace quenching ring adjustable welding tool and its use method |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN211192618U (en) | Semi-automatic welding device for stainless steel pipe fitting | |
| CN104959754B (en) | Automobile axle housing drain plug seat welding device | |
| CN101434006A (en) | Laser beam welding workstation | |
| CN220560721U (en) | Laser welding seam locating and tracking device | |
| CN110116285B (en) | An automatic gear welding mechanism | |
| CN213998420U (en) | Automatic pipe welding equipment | |
| CN210081016U (en) | Device for welding | |
| CN211029441U (en) | Automatic deflection polishing mechanism for pipe welding seam | |
| CN221454842U (en) | A guiding and positioning structure | |
| CN211277987U (en) | Jig for processing punch | |
| CN210360071U (en) | Automatic positioner product rotating device | |
| CN211029003U (en) | A clamping tool with flip function | |
| CN222242709U (en) | A four-axis hydraulic fixture for supporting body | |
| CN209953870U (en) | High-precision end socket beveling machine | |
| CN219521288U (en) | Novel drilling device for multi-bit drilling | |
| CN112548290A (en) | Semi-automatic plasma cutting annular groove processing device | |
| CN207239579U (en) | A kind of pipe fitting straight bead welding grips mobile device | |
| CN210360008U (en) | Traction machine base welding fixture | |
| CN213857797U (en) | A fully automatic small parts welding device | |
| CN210937240U (en) | A spherical dome automatic drilling machine | |
| CN210818120U (en) | Welding machine for water separator | |
| CN210937824U (en) | Automatic welding machine without spot welding | |
| CN220838708U (en) | Omnibearing multifunctional welding frame | |
| CN224129030U (en) | Part clamping device for machine manufacturing | |
| CN223406460U (en) | A hydraulic clamp for a machining center |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20210115 |
|
| WD01 | Invention patent application deemed withdrawn after publication |