WO2024224527A1 - リチウム2次電池 - Google Patents
リチウム2次電池 Download PDFInfo
- Publication number
- WO2024224527A1 WO2024224527A1 PCT/JP2023/016516 JP2023016516W WO2024224527A1 WO 2024224527 A1 WO2024224527 A1 WO 2024224527A1 JP 2023016516 W JP2023016516 W JP 2023016516W WO 2024224527 A1 WO2024224527 A1 WO 2024224527A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- secondary battery
- laminate
- mark
- lithium secondary
- metal sheet
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images







Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/05—Accumulators with non-aqueous electrolyte
- H01M10/058—Construction or manufacture
- H01M10/0585—Construction or manufacture of accumulators having only flat construction elements, i.e. flat positive electrodes, flat negative electrodes and flat separators
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M4/00—Electrodes
- H01M4/02—Electrodes composed of, or comprising, active material
- H01M4/64—Carriers or collectors
- H01M4/66—Selection of materials
- H01M4/665—Composites
- H01M4/667—Composites in the form of layers, e.g. coatings
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/05—Accumulators with non-aqueous electrolyte
- H01M10/052—Li-accumulators
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/05—Accumulators with non-aqueous electrolyte
- H01M10/052—Li-accumulators
- H01M10/0525—Rocking-chair batteries, i.e. batteries with lithium insertion or intercalation in both electrodes; Lithium-ion batteries
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/05—Accumulators with non-aqueous electrolyte
- H01M10/058—Construction or manufacture
- H01M10/0583—Construction or manufacture of accumulators with folded construction elements except wound ones, i.e. folded positive or negative electrodes or separators, e.g. with "Z"-shaped electrodes or separators
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M10/00—Secondary cells; Manufacture thereof
- H01M10/05—Accumulators with non-aqueous electrolyte
- H01M10/058—Construction or manufacture
- H01M10/0587—Construction or manufacture of accumulators having only wound construction elements, i.e. wound positive electrodes, wound negative electrodes and wound separators
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M4/00—Electrodes
- H01M4/02—Electrodes composed of, or comprising, active material
- H01M4/64—Carriers or collectors
- H01M4/66—Selection of materials
- H01M4/663—Selection of materials containing carbon or carbonaceous materials as conductive part, e.g. graphite, carbon fibres
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M4/00—Electrodes
- H01M4/02—Electrodes composed of, or comprising, active material
- H01M4/64—Carriers or collectors
- H01M4/66—Selection of materials
- H01M4/668—Composites of electroconductive material and synthetic resins
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M50/00—Constructional details or processes of manufacture of the non-active parts of electrochemical cells other than fuel cells, e.g. hybrid cells
- H01M50/50—Current conducting connections for cells or batteries
- H01M50/531—Electrode connections inside a battery casing
- H01M50/533—Electrode connections inside a battery casing characterised by the shape of the leads or tabs
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M50/00—Constructional details or processes of manufacture of the non-active parts of electrochemical cells other than fuel cells, e.g. hybrid cells
- H01M50/50—Current conducting connections for cells or batteries
- H01M50/531—Electrode connections inside a battery casing
- H01M50/534—Electrode connections inside a battery casing characterised by the material of the leads or tabs
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M50/00—Constructional details or processes of manufacture of the non-active parts of electrochemical cells other than fuel cells, e.g. hybrid cells
- H01M50/50—Current conducting connections for cells or batteries
- H01M50/531—Electrode connections inside a battery casing
- H01M50/536—Electrode connections inside a battery casing characterised by the method of fixing the leads to the electrodes, e.g. by welding
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M50/00—Constructional details or processes of manufacture of the non-active parts of electrochemical cells other than fuel cells, e.g. hybrid cells
- H01M50/50—Current conducting connections for cells or batteries
- H01M50/531—Electrode connections inside a battery casing
- H01M50/538—Connection of several leads or tabs of wound or folded electrode stacks
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01M—PROCESSES OR MEANS, e.g. BATTERIES, FOR THE DIRECT CONVERSION OF CHEMICAL ENERGY INTO ELECTRICAL ENERGY
- H01M50/00—Constructional details or processes of manufacture of the non-active parts of electrochemical cells other than fuel cells, e.g. hybrid cells
- H01M50/50—Current conducting connections for cells or batteries
- H01M50/531—Electrode connections inside a battery casing
- H01M50/54—Connection of several leads or tabs of plate-like electrode stacks, e.g. electrode pole straps or bridges
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/50—Manufacturing or production processes characterised by the final manufactured product
Definitions
- An exemplary embodiment of the present disclosure relates to a lithium secondary battery.
- Patent Document 1 discloses that the safety of battery cells is improved by using a current collector in which metal layers are formed on both sides of a resin film. The front and back of the resin film are separated by an insulating resin layer, and electrical conduction is not possible. Therefore, when connecting the electrode film to an electrode tab for drawing out wiring, conduction is not possible between the front and back of the electrode, or between multiple electrodes and the electrode tabs.
- Patent Document 2 discloses that the current collector is folded multiple times and laminated on each metal layer in order to connect each metal layer separated by a resin layer to the electrode tab for drawing out wiring.
- This disclosure provides technology that suppresses the decline in output characteristics and productivity of lithium secondary batteries.
- a lithium secondary battery includes: (a) a first laminate including a first current collector having a first insulating layer sandwiched between a pair of first conductive layers, and a first electrode disposed on the first current collector, the first current collector having a first end where the first electrode is not disposed; (b) an intermediate laminate including an electrode having a polarity different from that of the first electrode and a separator; and (c) a second laminate disposed in a stacking direction spaced apart from the first laminate via the intermediate laminate, the second current collector including a second insulating layer sandwiched between a pair of second conductive layers, and a second electrode disposed on the second current collector and having the same polarity as the first electrode, the second current collector being disposed on the second current collector.
- a lithium secondary battery includes: (d) a metal sheet arranged in parallel with the first and second ends in the stacking direction, the metal sheet including a first portion that overlaps with the first and second ends as viewed from the stacking direction, and a second portion that does not overlap with the first and second ends as viewed from the stacking direction; and (e) an electrode tab electrically connected to the first and second stacks, the electrode tab having a first bonding mark and a second bonding mark, the first bonding mark being a bonding mark between the electrode tab and the first end, the first portion and the second end of the metal sheet, and the second bonding mark being a bonding mark between the electrode tab and the second portion of the metal sheet.
- a technology can be provided that suppresses the deterioration of the output characteristics and productivity of lithium secondary batteries.
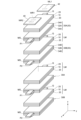
- FIG. 2 is an exploded perspective view for explaining a configuration example of a secondary battery 1.
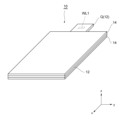
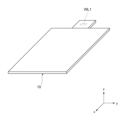
- FIG. 2 is a perspective view showing an example of a negative electrode 10.
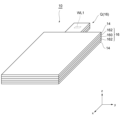
- FIG. 2 is a perspective view showing another example of the negative electrode 10.
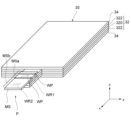
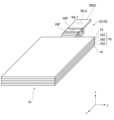
- FIG. 2 is a perspective view showing an example of a positive electrode laminate 30 and a metal sheet MS.
- FIG. 11 is a diagram for explaining an example of a joining mark.
- 13A and 13B are diagrams for explaining other examples of the joining marks.
- 13A and 13B are diagrams for explaining other examples of the joining marks.
- 13A and 13B are diagrams for explaining other examples of the joining marks.
- 13 is a diagram for explaining the joining state of a positive electrode tab 40, an end P, and a metal sheet MS.
- FIG. 4 is a diagram for explaining a first joining mark. 1 is a flow chart showing an example of the present manufacturing method.
- FIG. 8 is a diagram for explaining step ST1 in FIG. 7 .
- FIG. 8 is a diagram for explaining step ST2 in FIG. 7 .
- FIG. 8 is a diagram for explaining step ST2 in FIG. 7 .
- FIG. 8 is a diagram for explaining step ST2 in FIG. 7 .
- FIG. 8 is a diagram for explaining step ST2 in FIG. 7 .
- FIG. 8 is a diagram for explaining step ST2 in FIG. 7 .
- FIG. 8 is a diagram for explaining step ST3 in FIG. 7 .
- FIG. 2 is a perspective view showing another example of the negative electrode 10.
- FIG. 2 is a perspective view showing another example of the negative electrode 10.
- FIG. 2 is a perspective view showing another example of the negative electrode 10.
- FIG. 11 is a cross-sectional view of a main portion for explaining another example of the configuration of a lithium secondary battery.
- FIG. 11 is a cross-sectional view of a main portion for explaining another example of the configuration of a lithium secondary battery.
- FIG. 13 is a perspective view illustrating another example of the configuration of the positive electrode laminate.
- FIG. 13 is a perspective view illustrating another example of the configuration of the positive electrode laminate.
- a lithium secondary battery includes: (a) a first laminate including a first current collector having a first insulating layer sandwiched between a pair of first conductive layers, and a first electrode arranged on the first current collector, the first current collector having a first end where the first electrode is not arranged; (b) an intermediate laminate including an electrode having a polarity different from that of the first electrode and a separator; and (c) a second laminate arranged in a stacking direction spaced apart from the first laminate via the intermediate laminate, the second current collector including a second insulating layer sandwiched between a pair of second conductive layers, and a second electrode arranged on the second current collector and having the same polarity as the first electrode, the second current collector having a first end where the second electrode is not arranged.
- a lithium secondary battery includes: (d) a metal sheet arranged in parallel with the first and second ends in the stacking direction, the metal sheet including a first portion that overlaps with the first and second ends as viewed from the stacking direction, and a second portion that does not overlap with the first and second ends as viewed from the stacking direction; and (e) an electrode tab electrically connected to the first and second stacks, the electrode tab having a first bonding mark and a second bonding mark, the first bonding mark being a bonding mark between the electrode tab and the first end, the first portion and the second end of the metal sheet, and the second bonding mark being a bonding mark between the electrode tab and the second portion of the metal sheet.
- the first joining mark is a welding mark.
- the first bonding mark is in the form of one or more lines.
- the first bonding mark is in the form of one or more dots.
- the first bonding mark includes an area in a cross section in the stacking direction where a pair of first conductive layers, a metal sheet, and a pair of second conductive layers are integrated.
- the second joining mark is a welding mark.
- the second bonding mark is in the form of one or more lines.
- the second bonding mark is in the form of one or more dots.
- the first portion of the metal sheet further has a preliminary joining mark resulting from joining to either the first end or the second end.
- the first bonding mark is located at a different position from the preliminary bonding mark when viewed from the stacking direction.
- first and second laminates are arranged alternately in the stacking direction with an intermediate laminate in between.
- the first laminate is composed of a flat sheet
- the second laminate is composed of a flat sheet separate from the first laminate
- the first laminate and the second laminate are constructed by folding or rolling a single sheet.
- the metal sheet is provided at at least one of the plurality of first ends and the plurality of second ends.
- the metal sheet is provided on one side of at least one end.
- the metal sheets are provided on both sides of at least one end.
- the number of metal sheets is less than or equal to three times the total number of first ends and second ends.
- the metal sheet is constructed from the same material as the first conductive layer and the second conductive layer.
- the first electrode and the second electrode are positive electrodes.
- the first electrode and the second electrode are negative electrodes.
- Patent Document 2 proposes folding the current collector multiple times and stacking it on each metal layer in order to connect each metal layer separated by a resin layer to an electrode tab for drawing out wiring.
- this method requires a new device mechanism for stacking while folding back the end of the current collector for each metal layer.
- the end of the current collector must be folded back in conjunction with the stacking, which significantly reduces productivity.
- a lithium secondary battery 1 (hereinafter also referred to as "secondary battery 1") according to one embodiment can solve these problems.
- Fig. 1 is an exploded perspective view for explaining a configuration example of a secondary battery 1.
- the secondary battery 1 includes a negative electrode 10, a separator 20, a first positive electrode laminate 30A, a second positive electrode laminate 30B, a metal sheet MS, a positive electrode tab 40, and a negative electrode tab 42.
- a negative electrode 10 As shown in Fig. 1, the secondary battery 1 includes a negative electrode 10, a separator 20, a first positive electrode laminate 30A, a second positive electrode laminate 30B, a metal sheet MS, a positive electrode tab 40, and a negative electrode tab 42.
- (Negative electrode 10) 2A is a perspective view showing an example of the negative electrode 10.
- the negative electrode 10 includes a negative electrode current collector 12 and a negative electrode active material 14 disposed on the negative electrode current collector 12.
- the negative electrode active material 14 is disposed on both sides of the negative electrode current collector 12. In one embodiment, the negative electrode active material 14 may be disposed on only one side of the negative electrode current collector 12.
- the negative electrode current collector 12 is formed from at least one selected from the group consisting of metals that do not react with Cu, Ni, Ti, Fe, and Li, and alloys thereof, and stainless steel.
- the negative electrode active material 14 is a material that causes an electrode reaction, i.e., an oxidation reaction and a reduction reaction, at the negative electrode.
- the negative electrode active material 14 may be, for example, lithium metal and an alloy containing lithium metal, a carbon-based material, a metal oxide, a metal that alloys with lithium and an alloy containing the metal, etc.
- the carbon-based material may be, for example, graphene, graphite, hard carbon, carbon nanotubes, etc.
- the metal oxide may be, for example, a titanium oxide-based compound, a cobalt oxide-based compound, etc.
- the metal that alloys with lithium may be, for example, silicon, silicon oxide, germanium, tin, lead, aluminum, and gallium, and these may be pre-doped with lithium.
- FIG. 2B is a perspective view showing another example of the negative electrode 10.
- the negative electrode 10 may be configured to include a negative electrode collector 16 and a negative electrode active material 14 disposed on each side of the negative electrode collector 16.
- the material of the negative electrode active material 14 may be the same as that described in FIG. 2A.
- the negative electrode collector 16 may be configured to include a negative electrode insulating layer 160 and a pair of negative electrode conductive layers 162 disposed to sandwich the negative electrode insulating layer 160.
- the negative electrode insulating layer 160 may be composed of a sheet-like (film-like) or fibrous resin.
- the negative electrode conductive layer 162 is formed of at least one selected from the group consisting of metals that do not react with Cu, Ni, Ti, Fe, and Li, and alloys thereof, and stainless steel.
- the negative electrode conductive layer 162 is Cu.
- the negative electrode collector (12, 16) has a negative electrode end Q.
- the negative electrode end Q is configured as a part of the negative electrode collector, extending outward (in the x direction) from the side surface of the negative electrode collector.
- No negative electrode active material 14 is formed on the negative electrode end Q.
- a first bonding mark WL1 with the negative electrode tab 42 is formed on the negative electrode end Q.
- the negative electrode tabs 42 are arranged to be aligned in the stacking direction (z direction) with respect to each negative electrode end Q. In one embodiment, the negative electrode tabs 42 may be arranged above or below each negative electrode end Q. In one embodiment, the negative electrode tabs 42 may be arranged between a certain negative electrode end Q and an adjacent negative electrode end Q.
- the negative electrode tab 42 is joined to each negative electrode end Q.
- the negative electrode end 42 is electrically connected to each negative electrode 10 via each negative electrode end Q.
- a first joining mark WL1 is formed on the negative electrode tab 42 by joining with each negative electrode end Q.
- the first joining mark WL1 may be one or more points (spots), or may be a continuous line or surface.
- the negative electrode tab 42 and each negative electrode end Q may be joined by welding.
- the first joining mark WL1 is a welding mark.
- the welding may be, for example, ultrasonic welding, laser welding, resistance welding, or spot welding.
- the separator 20 is disposed on the negative electrode 10. In the example shown in FIG. 1, the separator 20 is disposed on both sides of the negative electrode 10. The separator 20 physically and/or electrically isolates the negative electrode 10 from the positive electrode laminate 30 and ensures ion conductivity of lithium ions.
- the separator 20 may be at least one selected from the group consisting of an insulating porous member, a polymer electrolyte, a gel electrolyte, and an inorganic solid electrolyte.
- the separator 20 may be a single member or a combination of two or more members.
- the separator 20 When the separator 20 includes an insulating porous member, the pores of the porous member are filled with a substance having ion conductivity (electrolyte, polymer electrolyte, and/or gel electrolyte, etc.). This allows the separator 20 to exhibit ion conductivity.
- a substance having ion conductivity electrolyte, polymer electrolyte, and/or gel electrolyte, etc.
- the separator 20 may be a porous polyethylene (PE) film, a porous polypropylene (PP) film, or a laminated structure thereof.
- the separator 20 may be coated on one or both sides with a separator coating layer. This may improve the cycle characteristics of the secondary battery 1.
- the separator coating layer may be a continuous film with a uniform thickness over 50% or more of the surface area of the separator 20.
- the separator coating layer may include a binder such as polyvinylidene fluoride (PVDF), a mixture of styrene butadiene rubber and carboxymethyl cellulose (SBR-CMC), and polyacrylic acid (PAA).
- the separator coating layer may be formed by adding inorganic particles such as silica, alumina, titania, zirconia, or magnesium hydroxide to the binder.
- the thickness of the separator 20 (including the coating layer if the separator 20 includes the coating layer) may be 3.0 ⁇ m or more and 40 ⁇ m or less. This can reduce the volume occupied by the separator 20 while isolating the negative electrode 10 and the positive electrode laminate 30.
- the thickness of the separator 20 may be 5.0 ⁇ m or more, 7.0 ⁇ m or more, or 10 ⁇ m or more.
- the thickness of the separator 20 may be 30 ⁇ m or less, 20 ⁇ m or less, or 10 ⁇ m or less.
- the negative electrode 10 and the separator 20 constitute an intermediate laminate LM.
- the intermediate laminate LM may have a structure in which the separator 20, the negative electrode 10, and the separator 20 are laminated in this order in the stacking direction (z direction).
- the secondary battery 1 includes a plurality of intermediate laminates LM.
- the plurality of intermediate laminates LM may each be configured as a single flat sheet as shown in FIG. 1.
- the plurality of intermediate laminates LM may be configured as a single sheet (an example of this embodiment will be described later with reference to FIG. 13 and FIG. 14).
- the first positive electrode laminate 30A includes a current collector 32A and a positive electrode 34A.
- the first positive electrode laminate 30A is an example of a first laminate.
- the first positive electrode laminate may have a structure in which a positive electrode 34A, a current collector 32A, and a positive electrode 34A are laminated in this order in the lamination direction.
- the current collector 32A has a first end P1 exposed from the positive electrode 34A. That is, the positive electrode 34A is not formed on the first end P1.
- the first end P1 extends outward (in the x direction) from the side surface of the current collector 32A as a part of the current collector 32A.
- the second positive electrode laminate 30B includes a current collector 32B and a positive electrode 34B.
- the second positive electrode laminate 30B is an example of a second laminate.
- the second positive electrode laminate 30B may have a structure in which a positive electrode 34B, a current collector 32B, and a positive electrode 34B are laminated in this order in the stacking direction.
- the current collector 32B has a second end P2 exposed from the positive electrode 34B.
- the positive electrode 34B is not formed on the second end P2.
- the second end P2 extends outward (in the x direction) from the side surface of the current collector 32B as part of the current collector 32B.
- the first positive electrode laminate 30A and the second positive electrode laminate 30B are alternately laminated in the stacking direction via the intermediate laminate LM (hereinafter, when there is no need to distinguish between the first positive electrode laminate 30A and the second positive electrode laminate 30B, they are collectively referred to as the "positive electrode laminate 30").
- the multiple positive electrode laminates 30 may each be configured as a single flat sheet as shown in FIG. 1.
- the multiple positive electrode laminates 30 may be configured as a single sheet (an example of this embodiment will be described later with reference to FIG. 15 and FIG. 16).
- the total number of positive electrode laminates 30 included in the secondary battery 1 may be 5 or more, 10 or more, or 20 or more. In one embodiment, the total number of positive electrode laminates 30 included in the secondary battery 1 may be 50 or less, 40 or less, or 30 or less. In one embodiment, the energy density of the secondary battery 1 may be 300 Wh/kg or more. In one embodiment, the rated capacity of the secondary battery 1 may be 1.5 Ah or more, or may be 5 Ah or more.
- the metal sheet MS is placed on the first end P1 and the second end P2 (hereinafter, when there is no need to distinguish between the two, they will be collectively referred to as "ends P").
- the metal sheet MS may be placed on all of the ends P.
- the metal sheet MS may be placed on some of the ends P, and no metal sheet MS may be placed on the remaining ends P.
- the metal sheet MS may be placed every several ends P.
- the number and thickness of metal sheets to be placed on an end P may be set based on the position of the end P in the stacking direction. For example, two or more metal sheets MS may be placed on the end P in the center of the stacking direction of the secondary battery 1, and one metal sheet MS may be placed on each of the end Ps at the top and bottom of the stacking direction. Also, for example, the thickness of the metal sheet MS placed on the end P in the center of the stacking direction of the secondary battery 1 may be made greater than the thickness of the metal sheet placed on each of the end Ps at the top and bottom of the stacking direction. This can suppress the variation in resistance between the central end Ps.
- the number of metal sheets MS may be three times or less than the total number of end parts P, or may be two times or less. In one embodiment, the number of metal sheets MS may be the same as the total number of end parts P, or may be less than the total number of end parts P, for example, less than half the total number of end parts P.
- FIG. 3 is a perspective view showing an example of a positive electrode laminate 30 and a metal sheet MS.
- the positive electrode laminate 30 may have a current collector 32 and positive electrodes 34 disposed on both sides of the current collector 32.
- the current collector 32 has an insulating layer 320 and conductive layers 322 formed to sandwich the insulating layer 320.
- the insulating layer 320 of the current collector 32 may be composed of, for example, a sheet-like (film-like) or fibrous resin.
- the resin may be, for example, at least one of polyolefin resins such as polyethylene terephthalate (PET), polyethylene, and polypropylene, and thermoplastic resins such as polystyrene, polyvinyl chloride, and polyamide.
- the insulating layer 320 may be composed of at least one of the resins laminated in multiple layers.
- the insulating layer 320 is formed from a material having a melting point of 150°C or higher and 300°C or lower.
- the thickness of the insulating layer 320 may be 3 ⁇ m or higher and 10 ⁇ m or lower, or 4 ⁇ m or higher and 8 ⁇ m or lower.
- the insulating layer 320 can function to melt in the event of abnormal heat generation due to overcharging or high temperature conditions, damaging the positive electrode laminate 30 and cutting off the short-circuit current inside the battery. This can suppress a sudden increase in temperature inside the secondary battery 1 and suppress the battery from catching fire. In other words, the insulating layer 320 can contribute to improving the safety of the secondary battery 1.
- the conductive layers 322 of the current collector 32 are formed on both sides of the insulating layer 320 so as to sandwich the insulating layer 320.
- the conductive layers 322 are in physical and/or electrical contact with the positive electrode 34 and function to give and receive electrons to and from the positive electrode 34.
- the conductive layers 322 are made of a conductor that does not react with lithium ions in a battery.
- the conductive layers 322 are made of at least one material selected from the group consisting of aluminum, titanium, stainless steel, nickel, and alloys thereof.
- the conductive layers 322 are aluminum or an aluminum alloy.
- the conductive layers 322 are formed by vapor deposition, sputtering, electrolytic plating, or lamination of the above material on the surfaces of both sides of the insulating layer 320.
- the thickness of each conductive layer 322 may be 0.5 ⁇ m to 5 ⁇ m, 0.7 ⁇ m to 3 ⁇ m, or 0.8 ⁇ m to 2.0 ⁇ m.
- the positive electrodes 34 are formed on both sides of the current collector 32.
- a known material may be appropriately selected as the positive electrodes 34 depending on the application.
- the thickness of the positive electrodes 34 may be appropriately adjusted depending on the desired capacity and rate characteristics of the battery. In one embodiment, the thickness of each positive electrode 34 is, for example, 20 ⁇ m or more and 150 ⁇ m or less.
- the positive electrode 34 has a positive electrode active material.
- the positive electrode active material is a material for holding the carrier metal in the positive electrode 34, and can also be called a host material for the carrier metal.
- the positive electrode active material may be a material for holding lithium ions in the positive electrode 34, in which case lithium ions are loaded into and deloaded from the positive electrode active material as the battery is charged and discharged. This can improve the stability and output voltage of the battery.
- the positive electrode active material is a metal oxide or a metal phosphate.
- the metal oxide may be, for example, a cobalt oxide-based compound, a manganese oxide-based compound, or a nickel oxide-based compound.
- the metal phosphate may be, for example, an iron phosphate-based compound or a cobalt phosphate-based compound.
- the positive electrode active material may be used alone or in combination of two or more.
- the content of the positive electrode active material in the positive electrode 34 may be 50 mass % or more and 100 mass % or less with respect to the entire positive electrode 34.
- the positive electrode 34 may contain one or more components other than the positive electrode active material.
- the positive electrode 34 may include a sacrificial positive electrode material. This is a lithium-containing compound that undergoes an oxidation reaction and does not substantially undergo a reduction reaction in the charge/discharge potential range of the positive electrode active material.
- the positive electrode 34 may include a gel electrolyte.
- the gel electrolyte may improve the adhesion between the positive electrode 34 and the current collector 32.
- the gel electrolyte includes a polymer, an organic solvent, and a lithium salt.
- the polymer in the gel electrolyte may be, for example, a copolymer of polyethylene and/or polyethylene oxide, polyvinylidene fluoride, and a copolymer of polyvinylidene fluoride and hexafluoropropylene.
- the positive electrode 34 may include a conductive additive and/or a binder.
- the conductive additive is carbon black, single-walled carbon nanotubes (SWCNT), multi-walled carbon nanotubes (MWCNT), carbon nanofibers (CF), or the like.
- the binder is polyvinylidene fluoride, polytetrafluoroethylene, styrene butadiene rubber, acrylic resin, polyimide resin, or the like.
- the content of the conductive additive is 0.5% to 30% by mass or less with respect to the entire positive electrode 34. In one embodiment, the content of the binder may be 0.5% to 30% by mass or less with respect to the entire positive electrode 34.
- the positive electrode 34 may include a polymer electrolyte.
- the polymer electrolyte is a solid polymer electrolyte that mainly includes a polymer and an electrolyte, and a semi-solid polymer electrolyte that mainly includes a polymer, an electrolyte, and a plasticizer.
- the total content of the polymer electrolyte may be 0.5% by mass to 30% by mass or less with respect to the entire positive electrode 34.
- the metal sheet MS may be joined to one surface of the end P of the current collector 32 (one surface of the pair of conductive layers 322). In one embodiment, the metal sheet MS may be joined to the other surface of the end P of the current collector 32 (the other surface of the pair of conductive layers 322). In one embodiment, one or more metal sheets MS may be provided at the end P. For example, one metal sheet MS may be joined to each of one surface and the other surface of the end P of the current collector 32.
- the metal sheet MS includes a first portion MSa and a second portion MSb.
- the first portion MSa is a portion that overlaps with the end P when viewed from the stacking direction (z direction).
- the second portion MSb is a portion that does not overlap with the end P when viewed from the stacking direction (z direction).
- the second portion MSb is a portion that extends outward (x direction) from the first portion MSa.
- a preliminary joining mark WP is formed between the first portion MSa of the metal sheet MS and the end P by joining the metal sheet MS and the end P.
- the preliminary joining mark WP may be a joining mark by welding, i.e., a welding mark.
- the welding may be, for example, ultrasonic welding, laser welding, resistance welding, or spot welding. In one example, the welding is ultrasonic welding.
- the metal sheet MS and the conductive layer 322 of the end P may be integrated by being fused in part or in whole at the preliminary joining mark WP by heat or the like.
- a first joint mark WR1 is formed on the first portion MSa and end P of the metal sheet MS.
- a second joint mark WR2 is formed on the second portion MSb of the metal sheet MS.
- the first joint mark WR1 is a joint mark between the end P and the metal sheet MS and the positive electrode tab 40
- the second joint mark WR2 is a joint mark between the metal sheet MS and the positive electrode tab 40.
- the preliminary joint mark WP, the first joint mark WR1, and the second joint mark WR2 are each formed at different positions from each other when viewed from the stacking direction (z direction).
- the metal sheet MS may be configured to cover only a part of the end P of the current collector 32, not the whole.
- the metal sheet MS may be disposed at a position spaced a predetermined distance from the positive electrode 34.
- an insulating layer may be provided in the area on the conductive layer 322 of the end P where the metal sheet MS is not disposed. In this case, in the event that the separator 20 is damaged, etc., the negative electrode 10 is prevented from shorting to the positive electrode 34 via the conductive layer 322 of the end P and/or the metal sheet MS, and the safety of the secondary battery 1 can be improved.
- the insulating layer may be, for example, a sheet-shaped (film-shaped) or fibrous resin.
- the resin may be, for example, at least one of polyolefin resins such as polyethylene terephthalate (PET), polyethylene, and polypropylene, and thermoplastic resins such as polystyrene, polyvinyl chloride, and polyamide.
- the metal sheet MS may be configured to cover the entire surface of the end P of the current collector.
- the metal sheet MS is made of at least one material selected from the group consisting of aluminum, titanium, stainless steel, nickel, and alloys thereof.
- the metal sheet MS is hard aluminum foil.
- the metal sheet MS is soft aluminum foil.
- the soft aluminum foil may be formed by subjecting the hard aluminum foil to a high-temperature (around 400°C) heat treatment.
- the metal sheet MS may be made of the same material as the conductive layer 322.
- the thickness of the metal sheet MS may be 3 ⁇ m or more, 5 ⁇ m or more, or 7 ⁇ m or more. In one embodiment, the thickness of the metal sheet MS may be 15 ⁇ m or less, 12 ⁇ m or less, or 10 ⁇ m or less.
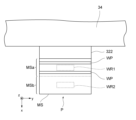
- FIG. 4A is a diagram for explaining an example of a bonding mark.
- FIG. 4A is a plan view of the vicinity of end P of the positive electrode laminate 30 shown in FIG. 3.
- the preliminary bonding marks WP may be formed in multiple lines (e.g., two lines) along the width direction (y direction) of the end P.
- the preliminary bonding marks WP are formed at a different position from the first bonding mark WR1 and the second bonding mark WR2 when viewed from the stacking direction.
- the preliminary bonding mark WP, the first bonding mark WR1, and the second bonding mark WR2 do not overlap each other in a planar view.
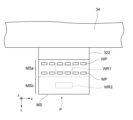
- FIGS. 4B to 4D are diagrams for explaining other examples of bonding marks.
- the first bonding marks WR1 may be formed in a line along the width direction (y direction) of the end P as shown in FIG. 4B.
- the first bonding marks WR1 may be in the form of multiple dots as shown in FIG. 4C and FIG. 4D, and may be formed in a line (FIG. 4C) or multiple lines (FIG. 4C) along the width direction (y direction) of the end P.
- the preliminary bonding marks WP are disposed at different positions from the first bonding marks WR1 and the second bonding marks WR2 when viewed from the stacking direction. That is, in any of FIG. 4B to FIG. 4D, the preliminary bonding marks WP, the first bonding marks WR1, and the second bonding marks WR2 do not overlap each other in a plan view.
- the positive electrode tab 40 is arranged to be aligned in the stacking direction (z direction) with respect to each end P (P1, P2) of the current collector 32 (32A, 32B) and each metal sheet MS. In one embodiment, the positive electrode tab 40 may be arranged above or below the end P of each current collector 32 and each metal sheet MS. In one embodiment, the positive electrode tab 40 may be arranged between a certain end P and an end P adjacent thereto.
- the positive electrode tab 40 is made of a conductive material.
- the positive electrode tab 40 may be made of, for example, aluminum or an aluminum alloy. In one example, the positive electrode tab 40 may be made of hard aluminum. In one embodiment, the thickness of the positive electrode tab 40 may be 0.05 mm or more and 1 mm or less, or 0.1 mm or more and 0.5 mm or less.
- the positive electrode tab 40 is joined to each end P of each collector 32 and each metal sheet MS. As a result, the positive electrode tab 40 is electrically connected to each positive electrode 34 via each end P. A first joint mark WR1 and a second joint mark WR2 are formed on the positive electrode tab 40.
- the first joint mark WR1 is a joint mark formed by joining the positive electrode tab 40 to each end P and the first portion MSa of each metal sheet MS.
- the first joint mark WR1 may be one or more points (spots) in a plan view, or may be a continuous line or surface.
- the first joint mark WR1 may be a joint mark formed by welding, i.e., a welding mark.
- the welding may be, for example, ultrasonic welding, laser welding, resistance welding, or spot welding. In one example, the welding is ultrasonic welding.
- the second joint mark WR1 is a joint mark formed by joining the positive electrode tab 40 and the second portion MSb of each metal sheet MS.
- the second joint mark WR2 may be one or more points (spots) in a plan view, or may be a continuous line or surface.
- the second joint mark WR2 may be a joint mark formed by welding, i.e., a welding mark.
- the welding may be, for example, ultrasonic welding, laser welding, resistance welding, or spot welding. In one example, the welding is ultrasonic welding.
- FIG. 5 is a diagram for explaining the bonding state of the positive electrode tab 40, the end P, and the metal sheet MS.
- FIG. 5 shows a schematic cross section of the end P, taken along the xz plane, at a location including the preliminary bonding mark WP, the first bonding mark WR1, and the second bonding mark WR2.
- the preliminary joining mark WP, the first joining mark WR1, and the second joining mark WR2 are provided at different positions from each other when viewed from the stacking direction.
- the preliminary joining mark WP is formed for each end P. In other words, one preliminary joining mark WP is not formed across multiple ends P.
- the first joining mark WR1 is formed over the positive electrode tab 40, each end P, and the entire first portion MSa of each metal sheet MS. That is, the first joining mark WR1 is formed continuously in the stacking direction from the positive electrode tab 40 to the end P of the bottom layer.
- the second joining mark WR2 is formed over the positive electrode tab 40 and the entire second portion MSb of each metal sheet MS. That is, the second joining mark WR2 is formed continuously from the positive electrode tab 40 to the second portion MSb of the bottom layer metal sheet MS.
- the second portion MSb of each metal sheet MS extends outward (in the x direction) further than the first portion MSa of the metal sheet MS joined to the end portion P.
- the thermal conductivity of the metal sheet MS tends to be higher than that of the end portion P, which includes an insulating layer 320 (e.g., resin, etc.). Therefore, heat from the end portion P (current collector 32) is transferred from the first portion MSa of the metal sheet MS to the second portion MSb outside it, and can be released to the outside from the second portion MSb directly or via the electrode tab 40. This allows heat generated inside the secondary battery 1 to be efficiently released to the outside. In other words, the heat dissipation properties of the secondary battery 1 can be improved.
- the second portions MSb of each metal sheet MS are joined to each other at the second joining mark WR2 without using the ends P (unlike the first portions MSa at the first joining mark WR1). That is, the joining area (second joining mark WR2) between the electrode tab 40 and the second portions MSb does not include the insulating layer 320 and is composed only of metal. Therefore, the resistance at the second joining mark WR2 can be kept low. This can improve the output characteristics of the secondary battery 1.
- FIG. 6 is a diagram for explaining the first bonding mark WR1.
- FIG. 6 shows a schematic cross section of the first bonding mark WR1 cut along the yz plane (cross section A-A in FIG. 5).
- the cross section of the first bonding mark WR1 includes a first region R1 and a second region R2.
- the cross section of the first bonding mark WR1 may have a recess recessed on one side in the stacking direction.
- the conductive layer 322 and the metal sheet MS are laminated integrally and joined to the positive electrode tab 40.
- being laminated integrally includes a state in which the conductive layers 322 and the metal sheet MS (first portion MSa) are partially or entirely fused together by heat or the like (a state in which the layers cannot be distinguished).
- the first region R1 may be substantially free of the insulating layer 320 along the stacking direction.
- the first region R1 provides a physical path for electrical connection between the electrode tab 40 and each of the conductive layers 322 and the metal sheet MS.
- the first region R1 may be configured between two second regions R2. In one embodiment, the maximum thickness of the first region R1 may be less than or equal to half the maximum thickness of the second region R2.
- the second region R2 a pair of conductive layers 322 sandwiching the insulating layer 320 and the metal sheet MS are laminated.
- the second region R2 is a region that includes the insulating layer 320 along the lamination direction.
- the first joint mark WR1 may be formed by welding.
- the first joint mark WR1 is a weld mark.
- the positive electrode tab 40, the end P, and the first portion MSa of the metal sheet MS may be pressed along the stacking direction. This causes the insulating layer 320 to soften at the welded location and be pushed outward in the width direction (left and right direction in FIG. 6) from the welded location.
- each conductive layer 322 and the metal sheet MS are thermally melted and integrated. This can form the first region R1 and the second region R2.
- the insulating layer 320 can suppress a sudden temperature rise inside the secondary battery 1 in the event of abnormal heat generation due to overcharge or high temperature conditions, and can suppress battery ignition.
- a collector having an insulating layer sandwiched between conductive layers As the number of collectors increases or the thickness of the insulating layers increases, it becomes more difficult to bond the end of the collector to the electrode tab and ensure stable bonding quality (variation control) in each layer. For example, if a strong force is applied in an attempt to weld the electrode tab to all the ends, the conductive layer at the end may be damaged or broken if the conductive layer is thin. On the other hand, if the electrode tab is welded with a force that does not damage the conductive layer, the bond may be insufficient and the resistance between the end of the collector and the electrode tab may increase.
- a metal sheet MS is disposed between at least one end P.
- the metal sheet MS functions as an additional conductive layer of the conductive layer 322 at the first joint mark WR1, and increases the ratio of the conductive layer to the insulating layer 320. Therefore, an increase in resistance at the first joint mark WR1 can be suppressed. This can improve the output characteristics of the secondary battery 1.
- the metal sheet MS can also function as a protective layer for the conductive layer 322 at the end P when the positive electrode tab 40 is joined to the end P.
- the resistance of the second bond mark WR2 may be 5.0 m ⁇ or less, 3.0 m ⁇ or less, 1.0 m ⁇ or less, or 0.5 m ⁇ or less.
- the secondary battery 1 may include an electrolytic solution.
- the electrolytic solution is a liquid containing a solvent and an electrolyte, and has ion conductivity.
- the electrolytic solution may be referred to as a liquid electrolyte, and acts as a conductive path for lithium ions. Therefore, when the secondary battery 1 includes the electrolytic solution, the internal resistance is reduced, and the energy density, capacity, and cycle characteristics can be improved.
- the electrolyte may be, for example, a solution that fills the case (pouch) of the secondary battery 1. Also, for example, the electrolyte may be impregnated into the separator 20, or may be held in a polymer to form a polymer electrolyte or a gel electrolyte.
- the electrolyte contained in the electrolytic solution may be, for example, a lithium salt.
- the lithium salt may be, for example, one or a combination of two or more selected from the group consisting of LiI , LiCl, LiBr, LiF , LiBF4 , LiPF6 , LiAsF6 , LiSO3CF3 , LiN( SO2F ) 2 , LiN ( SO2CF3 ) 2 , LiN( SO2CF3CF3 ) 2 , LiB( O2C2H4 ) 2 , LiB (C2O4) 2 , LiB (O2C2H4 ) F2 , LiB( OCOCF3 ) 4 , LiNO3, and Li2SO4 .
- non-aqueous solvents containing fluorine atoms (hereinafter referred to as "fluorinated solvents”) and non-aqueous solvents not containing fluorine atoms (hereinafter referred to as “non-fluorinated solvents”) may be added as solvents contained in the electrolyte solution.
- fluorinated solvents fluorine atoms
- non-fluorinated solvents non-aqueous solvents not containing fluorine atoms
- the fluorinated solvent may be, for example, 1,1,2,2-tetrafluoroethyl-2,2,3,3-tetrafluoropropyl ether, 1,1,2,2-tetrafluoroethyl-2,2,2-trifluoroethyl ether, and 1H,1H,5H-octafluoropentyl-1,1,2,2-tetrafluoroethyl ether.
- the non-fluorinated solvent may be, for example, triethylene glycol dimethyl ether, tetraethylene glycol dimethyl ether, 1,2-dimethoxyethane, dimethoxyethane, dimethoxypropane, dimethoxybutane, diethylene glycol dimethyl ether, acetonitrile, dimethyl carbonate, diethyl carbonate, ethyl methyl carbonate, ethylene carbonate, propylene carbonate, chloroethylene carbonate, methyl acetate, ethyl acetate, propyl acetate, methyl propionate, ethyl propionate, trimethyl phosphate, triethyl phosphate, and 12-crown-4.
- the above fluorinated solvents and/or non-fluorinated solvents may be used alone or in any combination of two or more in any ratio.
- the content of the fluorinated solvent and non-fluorinated solvent is not particularly limited, and the ratio of the fluorinated solvent to the total solvent may be 0 to 100% by volume, and the ratio of the non-fluorinated solvent to the total solvent may be 0 to 100% by volume.
- FIG. 7 is a flow chart showing an example of this manufacturing method.
- Figures 8A and 8B are views for explaining step ST1 in Figure 7.
- Figures 9A to 9D are views for explaining step ST2 in Figure 7.
- Figure 10 is a view for explaining step ST3 in Figure 7.
- this manufacturing method includes process ST1 of preparing a positive electrode laminate sheet, process ST2 of joining the metal sheets of the positive electrode laminate sheet, process ST3 of cutting out the positive electrode laminate sheet or the positive electrode laminate, process ST4 of assembling a molded body, process ST5 of joining the electrode tabs and the current collector, and process ST6 of sealing the molded body in an airtight container.
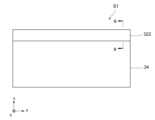
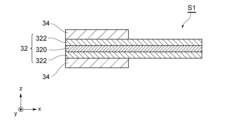
- a positive electrode laminate sheet S1 is prepared as shown in FIG. 8A and FIG. 8B.
- FIG. 8A is a plan view of the positive electrode laminate sheet S1.
- FIG. 8B is a cross-sectional view taken along line B-B of FIG. 8A.
- the positive electrode laminate sheet S1 may be a strip-shaped sheet having a longitudinal direction (y direction) and a lateral direction (x direction).
- the positive electrode laminate sheet S1 may be composed of a current collector 32 and a positive electrode 34 applied to both sides of the current collector 32 as shown in FIG. 8A and FIG. 8B.
- the current collector 32 may have an insulating layer 320 and a conductive layer 322 formed to sandwich the insulating layer 320. At one end of the lateral direction (x direction) of the positive electrode laminate sheet, the positive electrode 34 is not formed, and the conductive layer 322 of the current collector 32 is exposed.
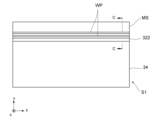
- step ST2 as shown in Figures 9A to 9D, a metal sheet MS is joined to one short end of the positive electrode laminate sheet S1.
- Figure 9A is a plan view of the positive electrode laminate sheet S1 to which the metal sheet MS is joined.
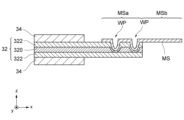
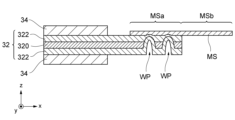
- Figures 9B to 9D are an example of a cross section taken along the line C-C of Figure 9A.
- the metal sheet MS is joined to the positive electrode laminate sheet S1 so as to have a portion (first portion MSa) that overlaps with one short-side end of the positive electrode laminate sheet S1 and a portion (second portion MSb) that extends in the short-side direction from the short-side end (see Figures 9B to 9D). Then, by the joining in process ST2, a preliminary joining mark WP is formed along the longitudinal direction, for example in a line shape (see Figure 9A).
- the metal sheet MS may be joined to the positive electrode laminate sheet S1 by welding.
- the welding may be, for example, ultrasonic welding, laser welding, resistance welding, or spot welding. In one example, the welding is ultrasonic welding.
- the joining in step ST2 may be performed by pressing the metal sheet MS against the current collector 32.
- the preliminary joining mark WP may be formed such that the first portion MSa of the metal sheet MS is recessed toward the current collector 32.
- the preliminary joining mark WP may be provided between the metal sheet MS and one conductive layer 322 (with which the metal sheet MS is in contact) as shown in FIG. 9B. In this case, at the preliminary joining mark WP, the metal sheet MS is not electrically connected to the other conductive layer 322.
- the preliminary joining mark WP may be provided between the metal sheet MS and both conductive layers 322 as shown in FIG. 9C. In this case, at the preliminary joining mark WP, the metal sheet MS is electrically connected to both conductive layers 322.
- the bonding in step ST2 may be performed by pressing the current collector 32 against the metal sheet MS.
- the preliminary bonding mark WP may be formed such that the current collector 32 is recessed toward the first portion MSa of the metal sheet MS.
- the metal sheet MS is electrically connected to both conductive layers 322.
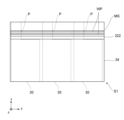
- step ST3 the positive electrode laminate 30 is cut out. Specifically, using a cutting blade, a laser, or the like, multiple positive electrode laminates 30 of a given shape are cut out from the positive electrode laminate sheet S1 in which the metal sheet MS is joined, as shown in FIG. 10. In this way, multiple positive electrode laminates 30 are obtained.
- step ST4 a molded body is assembled in which the positive electrode laminates 30 and intermediate laminates LM are alternately stacked.
- the multiple positive electrode laminates 30 prepared in step ST3 are arranged so as to be spaced apart from each other in the stacking direction via the intermediate laminates LM, as shown in FIG. 1.
- each positive electrode laminate 30 may be arranged between separators 20 formed by folding the sheet in a zigzag shape (see FIG. 9) or between separators 20 formed by rolling the sheet (see FIG. 10).
- step ST5 the electrode tabs and the current collectors are joined. Specifically, the end P of each current collector 32 and the metal sheet MS are joined to the electrode tab 40 so as to form the second joining mark WR2 described above. Also, the negative electrode end Q is joined to the negative electrode tab 42 so as to form the second joining mark WL2.
- the joining may be performed by ultrasonic welding, laser welding, resistance welding, or spot welding.
- step ST6 the molded body prepared in step ST5 is sealed in a sealed container.
- an electrolyte may be sealed in the sealed container.
- the sealed container may be, for example, a laminate film. In this manner, the secondary battery 1 is manufactured.
- step ST2 the metal sheet MS is preliminarily joined to the positive electrode laminate sheet MS. Therefore, in step ST3, the metal sheet MS can be simultaneously cut out to match the shape of the end P of the positive electrode laminate sheet S1. That is, a separate step of cutting the metal sheet MS to match the shape of the end P is not required.
- step ST5 it is not necessary to align the metal sheet MS with the end P of the current collector 32, so that the positive electrode tab 40 can be easily joined to the end P. Furthermore, in step ST5, it is theoretically possible to provide the first joining mark WR1 so that it does not overlap with the preliminary joining mark WP in the stacking direction.
- the joining state of the first joining mark WR1 is improved compared to when the two are provided overlapping, and an increase in the resistance of the first joining mark WR1 can be suppressed.
- the secondary battery 1 is charged and discharged by connecting the positive electrode tab 40 to one end of an external circuit and the negative electrode tab 42 to the other end of the external circuit.
- the external circuit may be, for example, a resistor, a power source, an apparatus, a device, another battery, or a potentiostat.
- the ends P of the multiple positive electrode laminates 30 may be connected to the external circuit at the same potential.
- the negative electrode ends Q of the multiple negative electrodes 10 may be connected to the external circuit at the same potential.
- the secondary battery 1 When a voltage is applied between the positive electrode tab 40 and the negative electrode tab 42 such that a current flows from the negative electrode tab 42 through an external circuit to the positive electrode tab 40, the secondary battery 1 is charged and lithium metal is precipitated on the negative electrode 10. When the positive electrode tab 40 and the negative electrode tab 42 of the charged secondary battery 1 are connected via a desired external circuit, the secondary battery 1 is discharged and the lithium metal in the negative electrode 10 is electrolytically dissolved.
- the secondary battery 1 may have a solid electrolyte interface layer (SEI layer) formed on the surface of the negative electrode 10 or the surface of the separator 20 (i.e., the interface between the negative electrode 10 and the separator 20) by the first charge (initial charge) after the battery is assembled.
- SEI layer may contain, for example, an inorganic compound containing lithium, or an organic compound containing lithium.
- the thickness of the SEI layer is 1.0 nm or more and 10 ⁇ m or less.
- the secondary battery 1 described above can improve the battery's output characteristics and productivity.
- the secondary battery 1 may be modified in various ways without departing from the scope and spirit of the present disclosure.
- Fig. 11 is a perspective view showing another example of the negative electrode 10.
- a metal sheet may be provided at the negative electrode end Q of the negative electrode 10.
- the example shown in Fig. 11 is an example in which a negative electrode metal sheet MS2 is provided on one surface of the negative electrode end Q of the negative electrode 10 shown in Fig. 2B.
- the negative electrode metal sheet MS2 may be made of the same material as the negative electrode conductive layer 162.
- the negative electrode metal sheet MS2 is Cu.
- a preliminary bonding mark WP may be formed between the negative electrode metal sheet MS2 and the negative electrode end Q by joining the negative electrode metal sheet MS2 and the negative electrode end Q.
- a first bonding mark WL1 may be formed by joining the negative electrode end Q and the negative electrode metal sheet MS2 to the negative electrode tab 42.
- a second bonding mark WL2 may be formed by joining the negative electrode metal sheet MS2 to the negative electrode tab 42.
- the bonding form and positional relationship of the preliminary bonding mark WP, first bonding mark WL1, and second bonding mark WL2 of the negative electrode end Q may be similar to the preliminary bonding mark WP, first bonding mark WR1, and second bonding mark WR2 at the end P described above, and a description thereof will be omitted.
- FIG. 12 is a perspective view showing another example of the negative electrode 10.
- the negative electrode 10 may be substantially free of a negative electrode active material.
- the negative electrode 10 is composed of at least one selected from the group consisting of Cu, Ni, Ti, Fe, and other metals that do not react with Li, and alloys thereof, as well as stainless steel (SUS).
- the "metal that does not react with Li” may be a metal that does not react with lithium ions or lithium metal to form an alloy when the secondary battery 1 is in an operating state.
- the negative electrode 10 also functions as a current collector.
- the negative electrode 10 being “substantially free of negative electrode active material” includes, for example, that the layer thickness of the negative electrode active material deposited on the negative electrode 10 at the end of discharge (e.g., a state in which the open circuit voltage of the battery is 2.5 V or more and 3.6 V or less) is 25 ⁇ m or less. In one embodiment, the layer thickness of the negative electrode active material at the end of discharge may be 20 ⁇ m or less, 15 ⁇ m or less, 10 ⁇ m or less, or 5 ⁇ m or less, or may be 0 ⁇ m.
- the secondary battery 1 can also be called an "anode-free lithium battery", a “zero anode lithium battery”, or an “anodeless lithium battery”.
- the negative electrode 10 does not have a negative electrode active material before the initial charge of the battery (the state from when the battery is assembled until the first charge). That is, the secondary battery 1 may be charged and discharged by depositing lithium metal on the negative electrode after the initial charge, and then electrolytically dissolving the deposited lithium metal. In this case, the volume and mass occupied by the negative electrode active material are suppressed, the volume and mass of the entire battery are reduced, and the energy density is, in principle, high.
- “lithium metal deposits on the negative electrode” includes not only lithium metal depositing on the surface of the negative electrode, but also lithium metal depositing on the surface of the solid electrolyte interface (SEI) layer and the surface or inside of the buffer functional layer, which will be described later.
- SEI solid electrolyte interface
- M3.0 / M4.2 may be 40% or less or 35% or less, where M4.2 is the mass of lithium metal deposited on the negative electrode at a voltage of 4.2 V and M3.0 is the same mass at a voltage of 3.0 V. In one embodiment, the ratio M3.0 / M4.2 may be 1.0% or more, 2.0% or more, 3.0% or more, or 4.0% or more.
- the thickness of the negative electrode 10 may be 1.0 ⁇ m or more and 30 ⁇ m or less. This reduces the volume occupied by the negative electrode 10 in the secondary battery 1, and improves the energy density.
- the thickness of the negative electrode 10 may be 2.0 ⁇ m or more and 20 ⁇ m or less, 2.0 ⁇ m or more and 18 ⁇ m or less, or 3.0 ⁇ m or more and 15 ⁇ m or less.
- the negative electrode 10 may be coated on at least a portion of the surface facing the positive electrode laminate 30 with a compound (hereinafter also referred to as "negative electrode coating agent") that includes an aromatic ring to which two or more elements selected from the group consisting of N, S, and O are independently bonded.
- the negative electrode coating agent can be held on the negative electrode 10 by the above elements being coordinately bonded to the metal atoms that constitute the negative electrode 10. According to this embodiment, the non-uniform deposition reaction of lithium metal on the surface of the negative electrode 10 can be suppressed, and the lithium metal deposited on the negative electrode 10 can be suppressed from growing in a dendritic shape.
- the negative electrode coating agent is coated on at least a portion of the surface of the negative electrode 10. In one embodiment, 10% or more of the surface area may have the negative electrode coating agent, or 20% or more, 40% or more, 60% or more, or 80% or more of the surface may have the negative electrode coating agent.
- the aromatic ring contained in the anode coating agent may be an aromatic hydrocarbon, such as benzene, naphthalene, azulene, anthracene, and pyrene, and a heteroaromatic compound, such as furan, thiophene, pyrrole, imidazole, pyrazole, pyridine, pyridazine, pyrimidine, and pyrazine.
- the aromatic ring is an aromatic hydrocarbon.
- the aromatic ring is benzene or naphthalene.
- the aromatic ring is benzene.
- the negative electrode coating agent may be configured with one or more nitrogen atoms bonded to an aromatic ring.
- the negative electrode coating agent may be a compound having a structure in which a nitrogen atom is bonded to an aromatic ring and, in addition to the nitrogen atom, one or more elements selected from the group consisting of N, S, and O are each independently bonded.
- the cycle characteristics of the battery may be improved.
- the negative electrode coating agent may be, for example, at least one selected from the group consisting of benzotriazole, benzimidazole, benzimidazole thiol, benzoxazole, benzoxazole thiol, benzothiazole, and mercaptobenzothiazole, and derivatives thereof.
- the negative electrode coating agent is at least one selected from the group consisting of benzotriazole, benzimidazole, benzoxazole, and mercaptobenzothiazole, and derivatives thereof.
- a porous or fibrous buffer functional layer may be provided between the negative electrode 10 and the separator 20.
- the buffer functional layer has a solid portion (including a gel portion) having ionic conductivity and electrical conductivity, and a pore portion formed by the gaps in the solid portion.
- lithium metal may be precipitated on the surface of the negative electrode 10 (the interface between the negative electrode 10 and the buffer functional layer) and/or inside the buffer functional layer (the surface of the solid portion of the buffer functional layer).
- (Intermediate laminate) 13 and 14 are cross-sectional views of a main part for explaining another example of the configuration of a lithium secondary battery.
- the negative electrode 10 and the separators 20 arranged on both sides of the negative electrode 10 may be configured as a single sheet SH.
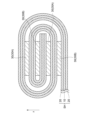
- the sheet SH is folded multiple times at acute angles to form an intermediate laminate, and each positive electrode laminate 30 (30A, 30B) may be disposed between the opposing separators 20 of the intermediate laminate.
- each positive electrode laminate 30 (30A, 30B) may be disposed between the opposing separators 20 of the intermediate laminate. Note that in the example shown in FIG. 14, each positive electrode laminate 30 may also be formed by winding a single sheet, as described below (see FIG. 15).
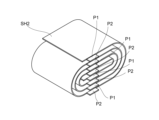
- each positive electrode laminate 30 may be configured by winding one sheet SH2 multiple times as shown in FIG. 15. In one embodiment, each positive electrode laminate 30 may be configured by folding one sheet SH2 alternately multiple times at acute angles as shown in FIG. 16.
- the sheet SH2 may be configured to include, for example, a current collector 32 and a positive electrode 34 disposed on both sides of the current collector 32. In the examples shown in FIG. 15 and FIG. 16, even if the current collector 32 and the positive electrode 34 are very thin, they can be handled as a single sheet SH2, so that the productivity of the battery can be improved.
- FIG. 17 shows the configurations and results of the examples and comparative examples.
- FIG. 18 shows the lamination patterns of the metal sheets in the examples and comparative examples. "Pattern 1" to “Pattern 4" in FIG. 18 correspond to "Pattern 1" to "Pattern 4" shown in "Lamination Pattern” in FIG. 17.
- Example 1 As Example 1, a lithium secondary battery having the structure shown in FIG. 1 was prepared. First, a negative electrode 10 having the structure shown in FIG. 2B was prepared. A 6 ⁇ m thick polyethylene terephthalate (PET) was used as the negative electrode insulating layer 160 of the negative electrode current collector 16, and 1.0 ⁇ m of Cu was evaporated as the negative electrode conductive layer 162. As the negative electrode active material 14, a mixed material was used in which 97 parts by mass of graphite, 0.5 parts by mass of carbon black as a conductive assistant, and 1.5 parts by mass of carboxymethyl cellulose (CMC) and 1.0 part by mass of styrene-butadiene rubber (SBR) as binders were mixed with water as a solvent.
- CMC carboxymethyl cellulose
- SBR styrene-butadiene rubber
- 21 negative electrodes 10 were prepared. Then, 21 metal sheets MS2 (copper foil having a thickness of 4 ⁇ m) for the negative electrode were prepared and attached to the negative electrode end Q of each negative electrode 10 by ultrasonic welding, resulting in the structure shown in FIG. 11. Next, a sheet (thickness: 15 ⁇ m) whose surface was coated with a mixture of polyvinylidene fluoride (PVDF) and Al 2 O 3 was prepared as the separator 20. Then, both sides of the negative electrode 10 were sandwiched and pressed with the separator 20 to obtain an intermediate laminate LM.
- PVDF polyvinylidene fluoride
- the current collector 32 of the positive electrode laminate 30 was a 6 ⁇ m-thick film-like polyethylene terephthalate (PET, insulating layer 320) on both sides of which Al (conductive layer 322) was vapor-deposited to a thickness of 1.0 ⁇ m.
- the positive electrode 34 was a mixture of 96 parts by mass of LiNi 0.8 Co 0.15 Al 0.05 O 2 as a positive electrode active material, 2 parts by mass of carbon black as a conductive assistant, and 2 parts by mass of polyvinylidene fluoride (PVDF) as a binder, in N-methyl-pyrrolidone (NMP) as a solvent.
- PVDF polyvinylidene fluoride
- the positive electrode 34 was applied to both sides of the current collector 32 with a basis weight of 23 mg/cm 2 , to obtain the positive electrode laminate 30. Twenty positive electrode laminates 30 were prepared. Further, 20 pieces of metal sheets MS (12 ⁇ m hard aluminum) were prepared and attached to the end P of the current collector 32 of each positive electrode laminate 30 by ultrasonic welding.
- the intermediate laminate LM and the positive electrode laminate 30 were alternately laminated. Then, each end P of the current collector 32 and the metal sheet MS were overlapped and joined to the positive electrode tab 40 by ultrasonic welding.
- the positive electrode tab 40 hard aluminum having a thickness of 0.2 mm was used.
- the negative electrode end Q and the metal sheet MS2 for the negative electrode were overlapped and joined to the negative electrode tab 42 by ultrasonic welding.
- the negative electrode tab 42 nickel-plated copper having a thickness of 0.2 mm was used. Such a structure was inserted into a laminate exterior body and sealed together with an electrolyte to obtain a lithium secondary battery.
- an electrolyte in which lithium hexafluorophosphate (LiPF 6 ) was dissolved in a solvent mixed with ethylene carbonate (EC), dimethyl carbonate (DMC), and ethyl methyl carbonate (EMC) in a ratio of 30:35:35 parts by mass to obtain 1M was used.
- Comparative Example 1 a lithium secondary battery was produced in the same manner as in Example 1, except that the metal sheet MS and the metal sheet MS2 for the negative electrode were not used.
- a metal sheet having only the first portion MSa i.e., not having the second portion MSb extending outward from the first portion MSa
- a metal sheet was provided at every other end (i.e., one for every two ends P and one for every two negative electrode ends Q) (i.e., the total number of metal sheets was half that of Example 1).
- a lithium secondary battery was created in the same manner as in Example 1.
- Example 1 Comparative Example 1, and Comparative Example 2
- positive electrode resistance the resistance between the positive electrode tab 40 and the positive electrode laminate 30
- the lithium secondary batteries according to the Example and Comparative Example were disassembled and measured by the four-terminal method.
- the positive electrode of the clip-type lead of a resistance meter BT3561 manufactured by HIOKI Corporation was connected to the positive electrode tab 40, and the negative electrode was clipped to one of the 20 positive electrode laminates 30 at a location where the positive electrode active material was not applied, and the impedance at 1 kHz was measured with the four-terminal lead.
- the negative electrode was connected to another positive electrode laminate and measurements were performed, and the average value of the 20 pieces was calculated.
- the resistance between the negative electrode tab 42 and the negative electrode 10 (hereinafter referred to as "negative electrode resistance”) was measured.
- the positive electrode resistance and negative electrode resistance of Example 1 were 0.48 m ⁇ and 0.62 m ⁇ , respectively. In contrast, the positive electrode resistance and negative electrode resistance of Comparative Example 1 were 22.3 m ⁇ and 19.4 m ⁇ , respectively. The positive electrode resistance and negative electrode resistance of Comparative Example 2 were 0.92 m ⁇ and 0.88 m ⁇ , respectively. The positive electrode resistance and negative electrode resistance of Example 1 were lower than those of Comparative Example 2 and significantly lower than those of Comparative Example 1.
- the nail penetration test is a test in which a nail is penetrated into each battery to simulate an internal short circuit, and the presence or absence of fire or explosion of the battery is confirmed.
- a lithium secondary battery (a) a first laminate including a first current collector having a first insulating layer sandwiched between a pair of first conductive layers, and a first electrode disposed on the first current collector, the first current collector having a first end portion where the first electrode is not disposed; (b) an intermediate laminate including an electrode having a polarity different from that of the first electrode and a separator; (c) a second laminate disposed in a stacking direction away from the first laminate via the intermediate laminate, the second laminate including a second current collector having a second insulating layer sandwiched between a pair of second conductive layers, and a second electrode disposed on the second current collector and having the same polarity as the first electrode, the second current collector having a second end where the second electrode is not disposed; (d) a metal sheet arranged in the stacking direction in parallel with the first end and the second end, the metal sheet including a first portion overlapping the first end and the second end as viewed from the stacking direction, and a
- 1...Lithium secondary battery 10...Negative electrode, 20...Separator, 30...Positive electrode laminate, 32...Current collector, 320...Insulating layer, 322...Conductive layer, 34...Positive electrode, 40...Positive electrode tab, 42...Negative electrode tab, MS...Metal sheet, MSa...First part, MSb...Second part, LM...Intermediate laminate, WR1...First bonding mark, WR2...Second bonding mark, WP...Preliminary bonding mark
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Materials Engineering (AREA)
- Composite Materials (AREA)
- Connection Of Batteries Or Terminals (AREA)
Priority Applications (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020257021546A KR20250112893A (ko) | 2023-04-26 | 2023-04-26 | 리튬 이차 전지 |
| JP2024572146A JP7752450B2 (ja) | 2023-04-26 | 2023-04-26 | リチウム2次電池 |
| CN202380093696.4A CN120660215A (zh) | 2023-04-26 | 2023-04-26 | 锂二次电池 |
| EP23935307.1A EP4704201A4 (en) | 2023-04-26 | 2023-04-26 | LITHIUM SECONDARY BATTERY |
| PCT/JP2023/016516 WO2024224527A1 (ja) | 2023-04-26 | 2023-04-26 | リチウム2次電池 |
| US19/358,000 US20260038988A1 (en) | 2023-04-26 | 2025-10-14 | Lithium secondary battery |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/JP2023/016516 WO2024224527A1 (ja) | 2023-04-26 | 2023-04-26 | リチウム2次電池 |
Related Child Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| US19/358,000 Continuation US20260038988A1 (en) | 2023-04-26 | 2025-10-14 | Lithium secondary battery |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2024224527A1 true WO2024224527A1 (ja) | 2024-10-31 |
Family
ID=93256099
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2023/016516 Ceased WO2024224527A1 (ja) | 2023-04-26 | 2023-04-26 | リチウム2次電池 |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20260038988A1 (cg-RX-API-DMAC7.html) |
| EP (1) | EP4704201A4 (cg-RX-API-DMAC7.html) |
| JP (1) | JP7752450B2 (cg-RX-API-DMAC7.html) |
| KR (1) | KR20250112893A (cg-RX-API-DMAC7.html) |
| CN (1) | CN120660215A (cg-RX-API-DMAC7.html) |
| WO (1) | WO2024224527A1 (cg-RX-API-DMAC7.html) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPWO2024252474A1 (cg-RX-API-DMAC7.html) * | 2023-06-05 | 2024-12-12 |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01102711A (ja) | 1987-10-15 | 1989-04-20 | Canon Electron Inc | 薄膜磁気ヘッド |
| JP2012129114A (ja) * | 2010-12-16 | 2012-07-05 | Sharp Corp | 非水系二次電池 |
| JP2012185938A (ja) * | 2011-03-03 | 2012-09-27 | Sharp Corp | 非水系二次電池 |
| JP2013016321A (ja) | 2011-07-01 | 2013-01-24 | Sharp Corp | 集電体および非水系二次電池 |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2011102711A (ja) | 2009-11-10 | 2011-05-26 | Konica Minolta Opto Inc | 球面収差評価方法 |
| EP2605313A1 (en) | 2011-12-15 | 2013-06-19 | Oxis Energy Limited | Connecting contact leads to lithium-based electrodes |
-
2023
- 2023-04-26 WO PCT/JP2023/016516 patent/WO2024224527A1/ja not_active Ceased
- 2023-04-26 JP JP2024572146A patent/JP7752450B2/ja active Active
- 2023-04-26 KR KR1020257021546A patent/KR20250112893A/ko active Pending
- 2023-04-26 EP EP23935307.1A patent/EP4704201A4/en active Pending
- 2023-04-26 CN CN202380093696.4A patent/CN120660215A/zh active Pending
-
2025
- 2025-10-14 US US19/358,000 patent/US20260038988A1/en active Pending
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01102711A (ja) | 1987-10-15 | 1989-04-20 | Canon Electron Inc | 薄膜磁気ヘッド |
| JP2012129114A (ja) * | 2010-12-16 | 2012-07-05 | Sharp Corp | 非水系二次電池 |
| JP2012185938A (ja) * | 2011-03-03 | 2012-09-27 | Sharp Corp | 非水系二次電池 |
| JP2013016321A (ja) | 2011-07-01 | 2013-01-24 | Sharp Corp | 集電体および非水系二次電池 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP4704201A1 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP4704201A4 (en) | 2026-06-24 |
| JPWO2024224527A1 (cg-RX-API-DMAC7.html) | 2024-10-31 |
| CN120660215A (zh) | 2025-09-16 |
| US20260038988A1 (en) | 2026-02-05 |
| EP4704201A1 (en) | 2026-03-04 |
| KR20250112893A (ko) | 2025-07-24 |
| JP7752450B2 (ja) | 2025-10-10 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US20250239622A1 (en) | Lithium secondary battery and method for manufacturing same | |
| JP7359491B2 (ja) | 電池及びその製造方法 | |
| JP7479104B1 (ja) | 電極シート及び2次電池 | |
| US12548759B2 (en) | Battery and method for producing same | |
| US20260038988A1 (en) | Lithium secondary battery | |
| JPH10112323A (ja) | 電 池 | |
| JP7573925B1 (ja) | リチウム2次電池及びリチウム2次電池の製造方法 | |
| JP7409762B2 (ja) | 非水電解液二次電池および非水電解液二次電池の製造方法 | |
| JP7492797B1 (ja) | リチウム2次電池 | |
| JP7784180B2 (ja) | リチウム2次電池 | |
| US20260088307A1 (en) | Secondary battery | |
| JP7498994B1 (ja) | リチウム2次電池 | |
| WO2025220215A1 (ja) | 2次電池 | |
| WO2025220213A1 (ja) | 2次電池 | |
| WO2025229751A1 (ja) | リチウム2次電池 | |
| WO2025243430A1 (ja) | リチウム2次電池、バッテリアセンブリ及び電動車 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 2024572146 Country of ref document: JP |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 23935307 Country of ref document: EP Kind code of ref document: A1 |
|
| WWP | Wipo information: published in national office |
Ref document number: 1020257021546 Country of ref document: KR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202380093696.4 Country of ref document: CN |
|
| WWP | Wipo information: published in national office |
Ref document number: 202380093696.4 Country of ref document: CN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202517101768 Country of ref document: IN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2023935307 Country of ref document: EP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| WWP | Wipo information: published in national office |
Ref document number: 202517101768 Country of ref document: IN |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| ENP | Entry into the national phase |
Ref document number: 2023935307 Country of ref document: EP Effective date: 20251126 |
|
| WWP | Wipo information: published in national office |
Ref document number: 2023935307 Country of ref document: EP |