WO2020189125A1 - カフユニット、カフユニットの製造方法、及び血圧測定装置 - Google Patents
カフユニット、カフユニットの製造方法、及び血圧測定装置 Download PDFInfo
- Publication number
- WO2020189125A1 WO2020189125A1 PCT/JP2020/005959 JP2020005959W WO2020189125A1 WO 2020189125 A1 WO2020189125 A1 WO 2020189125A1 JP 2020005959 W JP2020005959 W JP 2020005959W WO 2020189125 A1 WO2020189125 A1 WO 2020189125A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- cuff
- carla
- sheet
- air bag
- bag
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images











Classifications
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B5/00—Measuring for diagnostic purposes; Identification of persons
- A61B5/02—Detecting, measuring or recording for evaluating the cardiovascular system, e.g. pulse, heart rate, blood pressure or blood flow
- A61B5/021—Measuring pressure in heart or blood vessels
- A61B5/02141—Details of apparatus construction, e.g. pump units or housings therefor, cuff pressurising systems, arrangements of fluid conduits or circuits
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B5/00—Measuring for diagnostic purposes; Identification of persons
- A61B5/02—Detecting, measuring or recording for evaluating the cardiovascular system, e.g. pulse, heart rate, blood pressure or blood flow
- A61B5/021—Measuring pressure in heart or blood vessels
- A61B5/022—Measuring pressure in heart or blood vessels by applying pressure to close blood vessels, e.g. against the skin; Ophthalmodynamometers
- A61B5/02233—Occluders specially adapted therefor
- A61B5/02241—Occluders specially adapted therefor of small dimensions, e.g. adapted to fingers
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B5/00—Measuring for diagnostic purposes; Identification of persons
- A61B5/02—Detecting, measuring or recording for evaluating the cardiovascular system, e.g. pulse, heart rate, blood pressure or blood flow
- A61B5/021—Measuring pressure in heart or blood vessels
- A61B5/022—Measuring pressure in heart or blood vessels by applying pressure to close blood vessels, e.g. against the skin; Ophthalmodynamometers
- A61B5/0235—Valves specially adapted therefor
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B5/00—Measuring for diagnostic purposes; Identification of persons
- A61B5/68—Arrangements of detecting, measuring or recording means, e.g. sensors, in relation to patient
- A61B5/6801—Arrangements of detecting, measuring or recording means, e.g. sensors, in relation to patient specially adapted to be attached to or worn on the body surface
- A61B5/6802—Sensor mounted on worn items
- A61B5/681—Wristwatch-type devices
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B5/00—Measuring for diagnostic purposes; Identification of persons
- A61B5/68—Arrangements of detecting, measuring or recording means, e.g. sensors, in relation to patient
- A61B5/6801—Arrangements of detecting, measuring or recording means, e.g. sensors, in relation to patient specially adapted to be attached to or worn on the body surface
- A61B5/6843—Monitoring or controlling sensor contact pressure
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B2560/00—Constructional details of operational features of apparatus; Accessories for medical measuring apparatus
- A61B2560/04—Constructional details of apparatus
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B2562/00—Details of sensors; Constructional details of sensor housings or probes; Accessories for sensors
- A61B2562/02—Details of sensors specially adapted for in-vivo measurements
- A61B2562/0247—Pressure sensors
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B2562/00—Details of sensors; Constructional details of sensor housings or probes; Accessories for sensors
- A61B2562/12—Manufacturing methods specially adapted for producing sensors for in-vivo measurements
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61B—DIAGNOSIS; SURGERY; IDENTIFICATION
- A61B5/00—Measuring for diagnostic purposes; Identification of persons
- A61B5/74—Details of notification to user or communication with user or patient; User input means
- A61B5/742—Details of notification to user or communication with user or patient; User input means using visual displays
Definitions
- the present invention relates to a cuff unit used in a blood pressure measuring device, a method for manufacturing the cuff unit, and a blood pressure measuring device.
- blood pressure measuring devices used for measuring blood pressure have been used as a means for checking the health condition not only in medical equipment but also in the home.
- the blood pressure measuring device for example, expands and contracts a cuff wrapped around the upper arm or wrist of a living body, and detects the pressure of the cuff with a pressure sensor to detect the vibration of the arterial wall and measure the blood pressure.
- a cuff used in such a blood pressure measuring device for example, as disclosed in Japanese Patent Application Laid-Open No. 11-309119, a technique of inflating a plurality of air bags to compress an artery is known (for example, , Patent Document 1).
- the sensing cuff expands in the direction of pressure closure of the blood vessel, and the sensing cuff is required to come into close contact with the wrist when inflated. Therefore, in order to bring the inflated sensing cuff into close contact with the wrist, there is known a technique of using a carla between the belt for fixing the blood pressure measuring device to the wrist and the sensing cuff.
- such a blood pressure measuring device may have a configuration in which a pressing cuff that presses the sensing cuff against the wrist is fixed to the inner peripheral surface of the carla in order to bring the sensing cuff into close contact with the wrist.
- an object of the present invention is to provide a cuff unit capable of suppressing the displacement of the pressing cuff and the sensing cuff with respect to the carla, a method for manufacturing the cuff unit, and a blood pressure measuring device.
- a cuff unit including a sensing cuff formed in a second bag-shaped structure and including a joining allowance joined to the first bag-shaped structure adjacent to the second bag-shaped structure.
- the cuff includes a one- or multi-layered bag-like structure that is wrapped around the wrist or the like of a living body when measuring blood pressure and expands by being supplied with a fluid.
- the bag-shaped structure expands by a fluid, and when the fluid is air, it is an air bag.
- the pressing cuff and the sensing cuff can be fixed to the carla as an integral body. .. Therefore, since the pressing cuff and the sensing cuff can be fixed by one attachment work to the carla, the position of the pressing cuff and the sensing cuff to the carla is compared with the configuration in which the pressing cuff and the sensing cuff are fixed to the carla separately. The deviation can be suppressed. Further, it is possible to prevent the expansion of the pressing cuff from being hindered by the joining allowance.
- the first bag-shaped structure is formed in a long shape in one direction
- the second bag-shaped structure is formed in a long shape in one direction
- the joining allowance is the same.
- a cuff unit formed at an outer edge portion along the longitudinal direction of the second bag-shaped structure and joined to the outer edge portion along the longitudinal direction of the first bag-shaped structure.
- the joining allowance is joined over a wide range of the first bag-shaped structure. As a result, it is possible to prevent water such as sweat from the user from entering between the pressing cuff and the sensing cuff.
- the cuff unit of the above aspect is provided in which the pressing cuff and the sensing cuff are curved according to the inner peripheral surface of the carla.
- a cuff unit which is arranged between the pressing cuff and the sensing cuff and includes the pressing cuff and a back plate joined to the sensing cuff.
- the integrated body of the pressing cuff, the back plate, and the sensing cuff can be fixed to the carla with a single attachment work, so that the number of manufacturing steps of the blood pressure measuring device can be reduced.
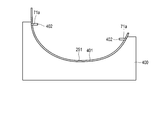
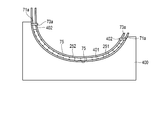
- the first structure including the pressing cuff is arranged on the previously described mounting surface of the jig having the mounting surface formed on the curved surface corresponding to the surface to which the pressing cuff of the carla is joined.
- the first structure is positioned with respect to the described surface
- a second structure including a sensing cuff is arranged on the first structure
- the second structure is positioned with respect to the previously described surface.
- Provided is a method for manufacturing a cuff unit, which joins and integrates a first structure and the second structure.
- the mounting surface formed on the curved surface corresponding to the surface on which the pressing cuff of the carla is fixed means that the cuff unit is the carla when the cuff unit formed along the mounting surface is fixed to the carla. It is a curved surface that can suppress the occurrence of wrinkles that inhibit expansion on at least one of the pressing cuff and the sensing cuff by being curved as compared with that before being fixed to.
- the curved surface of the carla corresponding to the surface on which the pressing cuff is arranged is, for example, a curved surface of the carla having the same curvature as the surface on which the pressing cuff is arranged.
- the curved surface of Carla corresponding to the surface on which the pressing cuff is placed is a curved surface of Carla having substantially the same curvature as the surface on which the pressing cuff is placed.
- the pressing cuff and the sensing cuff are integrally fixed by using a jig having a mounting surface formed on a curved surface corresponding to the surface on which the pressing cuff is fixed.
- the sensing cuff can be fixed integrally in a curved posture.
- the pressing cuff and the sensing cuff are integrally fixed by using a jig having a flat mounting surface to form a cuff unit
- the cuff unit is aligned with the flat mounting surface and the upper surface of the sensing cuff is adjusted. Is configured to be flat.
- the pressing cuff and the sensing cuff may be wrinkled due to the difference between the inner and outer circumferences caused by the cuff unit being curved according to the shape of the carla.
- the method for manufacturing a cuff unit is such that the second structure includes a joining allowance, and the first structure and the second structure are joined by the joining allowance. Provided.
- a method for manufacturing a cuff unit in which a second structure is arranged and the second structure is joined to the first structure and the back plate.
- the integrated body of the pressing cuff, the back plate, and the sensing cuff can be fixed to the carla with a single attachment work, so that the number of manufacturing steps of the blood pressure measuring device can be reduced.
- the jig has a plurality of positioning pins
- the first structure has a plurality of holes for arranging the positioning pins
- the second structure has the positioning pins.
- the joining allowance has a plurality of holes for arranging the positioning pins
- the plurality of positioning pins are set in the plurality of holes of the first structure and the plurality of holes of the second structure.
- the first structure and the second structure each include a cutting allowance, and the first structure and the second structure are fixed and integrated. Later, a method for manufacturing a cuff unit for cutting the cutting allowance is provided.
- the work efficiency of manufacturing the cuff unit can be improved by fixing and integrating the first structure and the second structure and then cutting.
- a carla and a plurality of first bag-like structures stacked and each inflated by a fluid are included, a pressing cuff joined to the carla, and one second bag-like structure inflated by the fluid.
- a cuff unit including a body and a sensing cuff formed on the second bag-shaped structure and joined to the first bag-shaped structure adjacent to the second bag-shaped structure, and the cuff unit.
- a blood pressure measuring device including a device main body for supplying the fluid.
- the pressing cuff and the sensing cuff can be fixed to the carla as an integral body. .. Therefore, since the pressing cuff and the sensing cuff can be fixed by one attachment work to the carla, the position of the pressing cuff and the sensing cuff to the carla is compared with the configuration in which the pressing cuff and the sensing cuff are fixed to the carla separately. The deviation can be suppressed. Further, it is possible to prevent the expansion of the pressing cuff from being hindered by the joining allowance.
- the present invention can provide a cuff unit capable of suppressing misalignment of the pressing cuff and the sensing cuff with respect to the carla, a method for manufacturing the cuff unit, and a blood pressure measuring device.
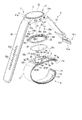
- FIG. 1 is a perspective view showing a configuration of a blood pressure measuring device according to an embodiment of the present invention.
- FIG. 2 is a perspective view showing the configuration of the blood pressure measuring device in an exploded manner.
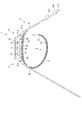
- FIG. 3 is a side view showing the configuration of the blood pressure measuring device.
- FIG. 4 is an explanatory view showing a state in which the blood pressure measuring device is worn on the wrist.
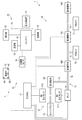
- FIG. 5 is a block diagram showing the configuration of the blood pressure measuring device.
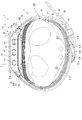
- FIG. 6 is a perspective view showing the configuration of the blood pressure measuring device.
- FIG. 7 is a perspective view showing the configurations of the carla and the cuff structure of the blood pressure measuring device in an exploded manner.
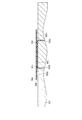
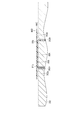
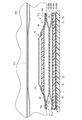
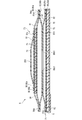
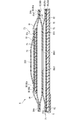
- FIG. 8 is a cross-sectional view showing the configuration of the carla and the cuff unit of the blood pressure measuring device.
- FIG. 9 is a cross-sectional view showing the configuration of the carla and the cuff unit of the blood pressure measuring device.
- FIG. 10 is a cross-sectional view showing the configuration of a tension cuff of the blood pressure measuring device.
- FIG. 11 is a cross-sectional view showing the configuration of a tension cuff of the blood pressure measuring device.
- FIG. 12 is a perspective view showing the configuration of Carla of the blood pressure measuring device.
- FIG. 13 is a plan view showing the configuration of the cuff structure of the blood pressure measuring device.
- FIG. 14 is a plan view showing the configuration of the cuff structure.
- FIG. 15 is a plan view showing the configuration of the pressing cuff of the blood pressure measuring device.
- FIG. 16 is a cross-sectional view showing the configuration of the pressing cuff.
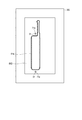
- FIG. 17 is a plan view showing a configuration of a sensing cuff of the blood pressure measuring device.
- FIG. 18 is a cross-sectional view showing the configuration of the sensing cuff.
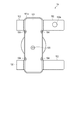
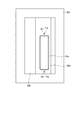
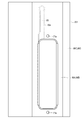
- FIG. 19 is a plan view showing the configuration of the cuff unit of the blood pressure measuring device.
- FIG. 20 is a plan view showing the configuration of a tension cuff of the blood pressure measuring device.
- FIG. 21 is a cross-sectional view showing the configuration of a tension cuff of the blood pressure measuring device.
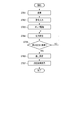
- FIG. 22 is a flow chart showing an example of a method for manufacturing the first structure.
- FIG. 22 is a flow chart showing an example of a method for manufacturing the first structure.
- FIG. 23 is a plan view showing the configuration of the first sheet.
- FIG. 24 is a plan view showing the configuration of the second sheet.
- FIG. 25 is a plan view showing the configuration of the third sheet.
- FIG. 26 is a plan view showing the configuration of the fourth sheet.
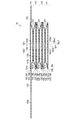
- FIG. 27 is an explanatory diagram showing an example of one step of the method for manufacturing the first structure.
- FIG. 28 is an explanatory diagram showing an example of one step of the manufacturing method of the first structure.
- FIG. 29 is an explanatory diagram showing an example of one step of the method for manufacturing the first structure.
- FIG. 30 is an explanatory diagram showing an example of one step of the method for manufacturing the first structure.
- FIG. 31 is an explanatory diagram showing an example of one step of the method for manufacturing the first structure.
- FIG. 32 is an explanatory diagram showing an example of one step of the method for manufacturing the first structure.
- FIG. 33 is an explanatory diagram showing an example of one step of the method for manufacturing the first structure.
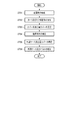
- FIG. 34 is a flow chart showing an example of a method for manufacturing the second structure.
- FIG. 35 is a plan view showing the configuration of the fifth sheet.
- FIG. 36 is a plan view showing the configuration of the sixth sheet.
- FIG. 37 is an explanatory diagram showing an example of one step of the method for manufacturing the second structure.
- FIG. 38 is an explanatory diagram showing an example of one step of the method for manufacturing the second structure.
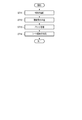
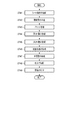
- FIG. 39 is a flow chart showing an example of a method for manufacturing a cuff unit.
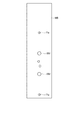
- FIG. 40 is a perspective view showing the configuration of the jig.
- FIG. 40 is a perspective view showing the configuration of the jig.
- FIG. 41 is an explanatory diagram showing an example of one step of the manufacturing method of the cuff unit.
- FIG. 42 is an explanatory diagram showing an example of one step of the manufacturing method of the cuff unit.
- FIG. 43 is an explanatory diagram showing an example of one step of the manufacturing method of the cuff unit.
- FIG. 44 is a flow chart showing an example of a method for manufacturing a tension cuff.
- FIG. 45 is a flow chart showing an example of a method for manufacturing the blood pressure measuring device.
- FIG. 46 is a flow chart showing an example of using the blood pressure measuring device.
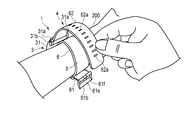
- FIG. 47 is a perspective view showing an example of wearing the blood pressure measuring device on the wrist.
- FIG. 48 is a perspective view showing an example of wearing the blood pressure measuring device on the wrist.
- FIG. 41 is an explanatory diagram showing an example of one step of the manufacturing method of the cuff unit.
- FIG. 42 is an explanatory diagram showing an example of one step of the manufacturing method of the
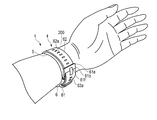
- FIG. 49 is a perspective view showing an example of wearing the blood pressure measuring device on the wrist.
- FIG. 50 is a cross-sectional view schematically showing a state in which the blood pressure measuring device is attached to the wrist.
- FIG. 51 is an explanatory diagram showing a modified example of one step of the manufacturing method of the cuff unit.
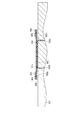
- FIG. 52 is a cross-sectional view showing a modified example of the cuff unit and the configuration of the carla.
- FIG. 53 is a cross-sectional view showing another modification of the cuff unit and the configuration of the carla.
- FIG. 1 is a perspective view showing the configuration of the blood pressure measuring device 1 according to the present embodiment.
- FIG. 2 is a perspective view showing the configuration of the blood pressure measuring device 1 in an exploded manner.
- FIG. 3 is a side view showing the configuration of the blood pressure measuring device 1.
- FIG. 4 is an explanatory view showing a state in which the blood pressure measuring device 1 is attached to the wrist 200.
- FIG. 5 is a block diagram showing the configuration of the blood pressure measuring device 1.
- FIG. 6 is a perspective view showing a part of the structure of the blood pressure measuring device 1 omitted.
- FIG. 7 is an exploded perspective view showing the configurations of the carla 5 and the cuff structure 6 of the blood pressure measuring device 1.
- FIG. 8 is a cross-sectional view showing the configuration of the carla 5 and the cuff unit 250 of the blood pressure measuring device 1.
- FIG. 9 is a cross-sectional view showing the configuration of the carla 5 and the cuff unit 250 of the blood pressure measuring device 1.
- FIG. 10 is a cross-sectional view showing the configuration of the tension cuff 74 of the blood pressure measuring device 1.
- FIG. 11 is a cross-sectional view showing the configuration of the tension cuff 74 of the blood pressure measuring device 1.
- FIG. 12 is a perspective view showing the configuration of the carla 5 of the blood pressure measuring device 1.
- FIG. 13 is a plan view showing the configuration of the cuff structure 6 of the blood pressure measuring device 1 on the wrist 200 side.
- FIG. 14 is a plan view showing the configuration of the cuff structure 6 on the inner peripheral surface side of the carla 5.
- FIG. 15 is a plan view showing the configuration of the pressing cuff 71 of the blood pressure measuring device 1.
- FIG. 16 is a cross-sectional view showing the configuration of the pressing cuff 71 in a cross section taken along line XVI-XVI in FIG.
- FIG. 17 is a plan view showing the configuration of the sensing cuff 73 of the blood pressure measuring device 1.
- FIG. 18 is a cross-sectional view showing the configuration of the sensing cuff 73 of the blood pressure measuring device 1 in a cross section taken along line XVIII-XVIII in FIG.
- FIG. 19 is a plan view showing the configuration of the cuff unit 250 of the blood pressure measuring device 1.
- FIG. 20 is a plan view showing the configuration of the tension cuff 74 of the blood pressure measuring device 1.
- FIG. 21 is a cross-sectional view showing the structure of the tension cuff 74.
- the blood pressure measuring device 1 is an electronic blood pressure measuring device worn on a living body.
- an electronic blood pressure measuring device having an aspect of a wearable device worn on the wrist 200 of a living body will be described.
- the blood pressure measuring device 1 includes a device main body 3, a belt 4 for fixing the device main body 3 to the wrist, a carla 5 arranged between the belt 4 and the wrist, and a pressing cuff 71.
- a cuff structure 6 having a sensing cuff 73 and a tension cuff 74, a fluid circuit 7 for fluidly connecting the device main body 3 and the cuff structure 6, and a power feeding unit 8 provided in the carla 5 are provided. ..
- the apparatus main body 3 includes, for example, a case 11, a display unit 12, an operation unit 13, a pump 14, a flow path unit 15, an on-off valve 16, and a pressure sensor 17.
- a power supply unit 18, a vibration motor 19, and a control board 20 are provided.
- the apparatus main body 3 supplies a fluid to the cuff structure 6 by means of a pump 14, an on-off valve 16, a pressure sensor 17, a control board 20, and the like.
- the case 11 includes a tubular outer case 31, a windshield 32 that covers an opening on the side opposite to the wrist 200 side (outer side) of the outer case 31, and an outer case 31. It includes a base 33 provided on the wrist 200 side inside, a back cover 35 covering the wrist 200 side of the outer case 31, and a seal member 36 provided on the lower surface of the back cover 35.
- the outer case 31 is formed in a cylindrical shape, for example.
- the outer case 31 includes a pair of lugs 31a provided at symmetrical positions in the circumferential direction of the outer peripheral surface, and a spring rod 31b provided between the two pairs of lugs 31a, respectively.
- the windshield 32 is, for example, a circular glass plate.
- the base 33 holds a display unit 12, an operation unit 13, a pump 14, an on-off valve 16, a pressure sensor 17, a power supply unit 18, a vibration motor 19, and a control board 20. Further, the base portion 33 constitutes, for example, a part of the flow path portion 15 that fluidly connects the pump 14 and the cuff structure 6.
- the back cover 35 is configured in an annular shape with the central side open.
- the back cover 35 covers the outer peripheral edge side of the end portion of the outer case 31 on the wrist 200 side.
- the central opening is covered by the carla 5, and together with the carla 5, a back cover that covers the end of the outer case 31 on the wrist 200 side is formed.
- the back cover 35 is fixed to the carla 5 by the four first fastening members 35a, and is fixed to the wrist 200-side end of the outer case 31 by the four second fastening members 35b.
- the back cover 35 is provided at the bottom portion, and is provided at four holes 35c through which the first fastening member 35a fixed to the carla 5 is inserted, and at four locations on the outer peripheral portion protruding in the radial direction. It has four holes 35d through which a second fastening member 35b fixed to the outer case 31 is inserted.
- the first fastening member 35a and the second fastening member 35b are members that mechanically fasten two parts such as screws, bolts, screws, and rivets.
- the first fastening member 35a and the second fastening member 35b are screws.
- the seal member 36 is, for example, a double-sided tape formed in the shape of a region of the back cover 35 in contact with the carla 5.
- the sealing member 36 exists between the carla 5 and the back cover 35 to seal between the carla 5 and the back cover 35.
- the display unit 12 is arranged on the base 33 of the outer case 31 and directly below the windshield 32. As shown in FIG. 5, the display unit 12 is electrically connected to the control board 20.
- the display unit 12 is, for example, a liquid crystal display or an organic electroluminescence display.
- the display unit 12 displays various information including the date and time, blood pressure values such as systolic blood pressure and diastolic blood pressure, and measurement results such as heart rate.
- the operation unit 13 is configured so that commands from the user can be input.
- the operation unit 13 is provided on a plurality of buttons 41 provided in the case 11, a sensor 42 for detecting the operation of the buttons 41, and a display unit 12 or a windshield 32. It includes a touch panel 43.
- the operation unit 13 converts a command into an electric signal by being operated by the user.
- the sensor 42 and the touch panel 43 are electrically connected to the control board 20, and output an electric signal to the control board 20.
- buttons 41 are provided.
- the button 41 is supported by the base 33 and projects from the outer peripheral surface of the outer case 31.
- the plurality of buttons 41 and the plurality of sensors 42 are supported by the base 33.
- the touch panel 43 is provided integrally with the windshield 32, for example.
- the pump 14 is, for example, a piezoelectric pump.
- the pump 14 compresses the air and supplies the compressed air to the cuff structure 6 through the flow path portion 15.
- the pump 14 is electrically connected to the control board 20.
- the flow path portion 15 constitutes a flow path connecting the pump 14 to the pressing cuff 71 and the tension cuff 74, and a flow path connecting the pump 14 to the sensing cuff 73. Further, the flow path portion 15 constitutes a flow path from the pressing cuff 71 and the tension cuff 74 to the atmosphere, and a flow path from the sensing cuff 73 to the atmosphere.
- the flow path portion 15 is an air flow path composed of a hollow portion, a groove, a flow path tank, a tube, and the like provided in the base portion 33 and the like.
- the on-off valve 16 opens and closes a part of the flow path portion 15.
- a plurality of on-off valves 16 are provided as shown in FIG. 5, as a specific example, and the flow path from the pump 14 to the pressing cuff 71 and the tension cuff 74 by the combination of opening and closing of each on-off valve 16 and the pump 14
- the flow path leading to the sensing cuff 73, the flow path connecting the pressing cuff 71 and the tension cuff 74 to the atmosphere, and the flow path connecting the sensing cuff 73 to the atmosphere are selectively opened and closed.
- the four on-off valves 16 are composed of a first on-off valve 16A, a second on-off valve 16B, a third on-off valve 16C, and a fourth on-off valve 16D.
- the first on-off valve 16A opens and closes the flow path connecting the pump 14 and the sensing cuff 73.
- the second on-off valve 16B opens and closes the flow path connecting the pump 14 and the tension cuff 74.
- the second on-off valve 16B and the third on-off valve 16C open and close the flow path connecting the pump 14 and the pressing cuff 71.
- the second on-off valve 16B, the third on-off valve 16C, and the fourth on-off valve 16D open and close the flow path connecting the pump 14 and the atmosphere.
- the pressure sensor 17 detects at least the pressure of the sensing cuff 73.
- the pressure sensor 17 includes, for example, a first pressure sensor 17A and a second pressure sensor 17B.
- the pressure sensor 17 converts the detected pressure into an electric signal and outputs it to the control board 20.
- the first pressure sensor 17A and the second pressure sensor 17B are provided in the flow path connecting the first pressure sensor 17A and the sensing cuff 73 of the flow path portion 15.
- the pressing cuff 71, the sensing cuff 73, the tension cuff 74, and the pump 14 are continuous by opening and closing each on-off valve, so that the pressure in these flow paths is connected to the pump 14, and the pressing cuff 71, the sensing cuff 73.
- the pressure in the internal space of the tension cuff 74 is the pressure in the internal space of the tension cuff 74.
- the pressure of the sensing cuff 73 when the first on-off valve 16A is open and the second on-off valve 16B is closed in other words, the flow connecting the pump 14 and the sensing cuff 73.
- the pressure of the road portion 15 is detected.
- the pressure of the sensing cuff 73 and the tension cuff 74 in other words, The pressure of the flow path portion 15 connecting the pump 14, the sensing cuff 73 and the tension cuff 74 is detected.
- the pressure sensor 17 has a pressing cuff 71, sensing when the first on-off valve 16A, the second on-off valve 16B and the third on-off valve 16C are open and the fourth on-off valve 16D is open or closed.
- the pressure of the cuff 73 and the tension cuff 74 in other words, the pressure of the flow path portion 15 connecting the pump 14, the pressing cuff 71, the sensing cuff 73 and the tension cuff 74 is detected.
- the power supply unit 18 is a secondary battery such as a lithium ion battery, for example.
- the power supply unit 18 is electrically connected to the control board 20 as shown in FIG.
- the power supply unit 18 supplies power to the control board 20.
- the control board 20 includes, for example, a board 51, an acceleration sensor 52, a communication unit 53, a storage unit 54, and a control unit 55.
- the control board 20 is composed of an acceleration sensor 52, a communication unit 53, a storage unit 54, and a control unit 55 mounted on the board 51.
- the substrate 51 is fixed to the base 33 of the case 11 with screws or the like.
- the acceleration sensor 52 is, for example, a 3-axis acceleration sensor.
- the acceleration sensor 52 outputs an acceleration signal representing acceleration in three directions orthogonal to each other of the device main body 3 to the control unit 55.
- the acceleration sensor 52 is used to measure the amount of activity of a living body equipped with the blood pressure measuring device 1 from the detected acceleration.
- the communication unit 53 is configured to be able to transmit and receive information wirelessly or by wire with an external device.
- the communication unit 53 transmits information controlled by the control unit 55 and information such as the measured blood pressure value and pulse to an external device via the network, and software from the external device via the network. Receives the update program, etc. and sends it to the control unit.
- the network is, for example, the Internet, but is not limited to this, and may be a network such as a LAN (Local Area Network) provided in the hospital, or a predetermined standard such as USB. It may be direct communication with an external device using a cable having a terminal or the like. Therefore, the communication unit 53 may be configured to include a plurality of wireless antennas, micro USB connectors, and the like.
- LAN Local Area Network
- USB Universal Serial Bus
- the storage unit 54 contains program data for controlling the entire blood pressure measuring device 1 and the fluid circuit 7, setting data for setting various functions of the blood pressure measuring device 1, and a blood pressure value and pulse from the pressure measured by the pressure sensor 17.
- the calculated data and the like for calculating the above are stored in advance.
- the storage unit 54 stores information such as the measured blood pressure value and pulse.
- the control unit 55 is composed of a single CPU or a plurality of CPUs, and controls the operation of the entire blood pressure measuring device 1 and the operation of the fluid circuit 7.
- the control unit 55 is electrically connected to the display unit 12, the operation unit 13, the pump 14, each on-off valve 16 and each pressure sensor 17, and supplies electric power. Further, the control unit 55 controls the operations of the display unit 12, the pump 14, and the on-off valve 16 based on the electric signals output by the operation unit 13 and the pressure sensor 17.
- the control unit 55 has a main CPU (Central Processing Unit) 56 that controls the operation of the entire blood pressure measuring device 1 and a sub CPU 57 that controls the operation of the fluid circuit 7.
- the main CPU 56 obtains a measurement result such as a blood pressure value such as systolic blood pressure and diastolic blood pressure and a heart rate from an electric signal output by the pressure sensor 17, and outputs an image signal corresponding to the measurement result to the display unit 12. .
- a measurement result such as a blood pressure value such as systolic blood pressure and diastolic blood pressure and a heart rate
- the sub CPU 57 drives the pump 14 and the on-off valve 16 to send compressed air to the pressing cuff 71 and the sensing cuff 73. Further, the sub CPU 57 controls the drive and stop of the pump 14 and the opening and closing of the on-off valve 16 based on the electric signal output from the pressure sensor 17. By controlling the pump 14 and the on-off valve 16, the sub CPU 57 selectively sends compressed air to the pressing cuff 71 and the sensing cuff 73, and selectively depressurizes the pressing cuff 71 and the sensing cuff 73.
- the belt 4 includes a first belt 61 provided on one pair of lugs 31a and a spring rod 31b, and a second belt 61 provided on the other pair of lugs 31a and a spring rod 31b.
- a belt 62 is provided. The belt 4 is wrapped around the wrist 200 via the carla 5.
- the first belt 61 is a so-called parent and is configured in a band shape that can be connected to the second belt 62. As shown in FIGS. 1 to 3, the first belt 61 has a belt portion 61a and a buckle 61b. The belt portion 61a is formed in a band shape. The belt portion 61a is made of an elastically deformable resin material. Further, the belt portion 61a has a flexible sheet-like insert member inside which expansion and contraction of the belt portion 61a in the longitudinal direction is suppressed. The belt portion 61a is formed at one end and has a first hole 61c orthogonal to the longitudinal direction of the belt 61a and a second hole 61c formed at the other end and orthogonal to the longitudinal direction of the first belt 61. It has 61d.
- the first hole portion 61c is provided at the end portion of the belt portion 61a.
- the first hole portion 61c has an inner diameter into which the spring rod 31b can be inserted and the first belt 61 can rotate with respect to the spring rod 31b. That is, the first belt 61 is rotatably held in the outer case 31 between the pair of lugs 31a and by arranging the first hole portion 61c in the spring rod 31b.
- the second hole portion 61d is provided at the tip of the belt portion 61a.
- a buckle 61b is attached to the second hole 61d.
- the buckle 61b has a rectangular frame-shaped frame-shaped body 61e and a stick 61f rotatably attached to the frame-shaped body 61e.
- One side of the frame-shaped body 61e to which the sticking rod 61f is attached is inserted into the second hole portion 61d, and the frame-shaped body 61e is rotatably attached with respect to the belt portion 61a.
- the second belt 62 is a so-called sword tip, and is formed in a band shape having a width that can be inserted into the frame-shaped body 61e.
- the second belt 62 is made of an elastically deformable resin material. Further, the second belt 62 has a sheet-like insert member inside which is flexible and suppresses expansion and contraction of the second belt 62 in the longitudinal direction.
- the second belt 62 has a plurality of small holes 62a into which the stick 61f is inserted. Further, the second belt 62 is provided at one end and has a third hole portion 62b orthogonal to the longitudinal direction of the second belt 62. The third hole portion 62b has an inner diameter into which the spring rod 31b can be inserted and the second belt 62 can rotate with respect to the spring rod 31b. That is, the second belt 62 is rotatably held in the outer case 31 between the pair of lugs 31a and by arranging the third hole portion 62b in the spring rod 31b.
- the second belt 62 is inserted into the frame-shaped body 61e, and the rod 61f attached to the small hole 62a is inserted, so that the first belt 61 and the second belt 62 are integrally connected to the outer shell. Together with the case 31, it forms an annular shape that follows the circumferential direction of the wrist 200.
- the belt 4 forms an annular shape that follows the circumferential direction of the wrist 200, thereby pressing the carla 5 and elastically deforming the carla 5 so as to follow the circumferential direction of the wrist of the wearer of the blood pressure measuring device 1.
- the carla 5 is formed in a band shape that curves along the circumferential direction of the wrist 200.
- the carla 5 is formed so that one end and the other end are separated from each other.
- the outer surface of the carla 5 on one end side is fixed to the back cover 35 of the apparatus main body 3.
- the carla 5 is arranged at a position where one end and the other end protrude toward one side of the wrist 200 with respect to the back cover 35.
- one end and the other end of the carla 5 are arranged on the side of the wrist 200.
- one end and the other end of the carla 5 are adjacent to each other at a predetermined distance.
- the carla 5 is made of, for example, a resin material.
- the carla 5 is formed of polypropylene to a thickness of about 1 mm.
- the carla 5 is configured in a band shape that curves along the circumferential direction of the wrist. Further, the carla 5 is provided at a position facing the back side of the wrist 200 on one end side, and is provided around the disc-shaped cover portion 5a and the cover portion 5a forming the back cover together with the back cover 35. It has a relief portion 5b that can move the second fastening member 35b that fixes the outer case 31 and the back cover 35.
- the cover portion 5a and a portion adjacent thereto are formed in a flat plate shape, and one end side and the other end side of the cover portion 5a are curved with a predetermined curvature.
- the carla 5 is formed so that the length from the cover portion 5a to one end is shorter than the length from the cover portion 5a to the other end.
- the short side from the cover portion 5a to one end is arranged on the back side of the wrist, and the longitudinal side from the cover portion 5a to the other end is one side from the back side of the wrist. It extends through to the palm side of the wrist 200.
- the carla 5 is formed in a shape in which the other end is located on the inner peripheral surface side of one end side when one end and the other end are close to each other.
- the width of the wrist 200 of the carla 5 in the width direction is set to be larger on the back side of the wrist 200 of the carla 5 than on the palm side of the wrist 200 of the carla 5.
- the radius of curvature of one end of the back side of the wrist 200 of the wrist 200 is set to be larger than the radius of curvature of the other end of the palm side of the wrist 200.
- the carla 5 is provided adjacent to the cover portion 5a on a part of the cover portion 5a, an outer surface on one end side from the cover portion 5a, and more specifically, an outer surface on the short side extending from the cover portion 5a.
- a recess 5c is provided.
- the cover portion 5a includes the inserted reinforcing insert member 5d.
- the cover portion 5a is fixed to the wrist 200 side of the outer case 31 via the fixed back cover 35.
- the cover portion 5a is provided at a position facing the four hole portions 35c of the back cover 35, and has a screw hole 5e into which the first fastening member 35a for fixing the back cover 35 is screwed. Further, the cover portion 5a has three hole portions 5f for connecting the cuff structure 6 to the apparatus main body 3.
- the relief portion 5b covers the second fastening member 35b without the second fastening member 35b interfering with the carla 5. It is a relief for arranging the tool 35 and for arranging the tool for rotating the second fastening member 35b.
- the three hole portions 5f have a first hole portion 5f1 formed to have an inner diameter into which the connection portion 84 described later in the pressing cuff 71 can be inserted, and a first hole portion 5f1 formed into an inner diameter into which the connecting portion 93 described later in the sensing cuff 73 can be inserted.
- the two-hole portion 5f2 and the third-hole portion 5f3 formed with an inner diameter into which the connection portion 103 described later of the tension cuff 74 can be inserted.
- the second hole portion 5f2 is arranged on the other end side of the palm side of the carla 5 in the cover portion 5a with respect to the first hole portion 5f1 and the third hole portion 5f3.
- Such a carla 5 is fixed to the outer case 31 with one end and the other end facing the second belt 62 of the belt 4. Further, the carla 5 has a cuff structure 6 facing the palm side of the wrist 200 by at least a position facing the palm side of the wrist 200 curved along the circumferential direction along the palm side of the wrist 200. , Hold in a curved state following the shape of the palm side of the wrist 200.
- the carla 5 has a hardness having flexibility and shape retention.
- flexibility means that the shape is deformed in the radial direction when an external force of the belt 4 is applied to the carla 5.
- flexibility means that when the carla 5 is pressed by the belt 4, the shape of the side view is deformed so as to be close to the wrist, follow the shape of the wrist, or follow the shape of the wrist.
- the shape retention means that the carla 5 can maintain a preformed shape when no external force is applied.
- the shape retention means that in the present embodiment, the shape of the carla 5 can be maintained in a curved shape along the circumferential direction of the wrist.
- the cuff structure 6 is arranged on the inner peripheral surface, and the cuff structure 6 is held along the shape of the inner peripheral surface of the carla 5.
- the pressing cuff 71 and the tension cuff 74 are arranged on the inner peripheral surface, and the cuff structure 6 is fixed by the bonding layer 75 provided between the carla 5 and the pressing cuff 71 and the tension cuff 74. By doing so, the cuff structure 6 is held.
- the bonding layer 75 is an adhesive or double-sided tape.
- the cuff structure 6 includes a pressing cuff 71, a back plate 72, a sensing cuff 73, and a tension cuff 74. Further, the cuff structure 6 includes a bonding layer 75 that joins each structure and the carla 5 and the cuffs 71 and 74. The cuff structure 6 is fixed to the carla 5. In the cuff structure 6, the pressing cuff 71, the back plate 72 and the sensing cuff 73 are laminated and arranged on the carla 5, and the tension cuff 74 is arranged on the carla 5 apart from the pressing cuff 71, the back plate 72 and the sensing cuff 73. Will be done.
- the cuff structure 6 has a pressing cuff 71 and a back on the inner peripheral surface of the wrist 200 of the carla 5 on the palm side, from the inner peripheral surface of the carla 5 toward the wrist 200.
- the plate 72 and the sensing cuff 73 are laminated and fixed in this order.
- the tension cuff 74 is arranged on the inner peripheral surface of the wrist 200 of the carla 5 on the back side of the hand.
- Each member of the cuff structure 6 is fixed to a member adjacent in the stacking direction by a joint layer 75.
- the pressing cuff 71 is fluidly connected to the pump 14 via the flow path portion 15.
- the pressing cuff 71 expands to press the back plate 72 and the sensing cuff 73 toward the wrist 200 side.
- the pressing cuff 71 is attached to a plurality of, for example, a two-layer air bag (first bag-shaped structure) 81 and an air bag 81 facing the carla 5.
- the jointed portion 82 provided, the flow path body 83 communicating with the air bag 81, and the connecting portion 84 provided at the tip of the flow path body 83 are included.
- Such a pressing cuff 71 is configured by integrally welding a plurality of sheet members 86.
- the air bag 81 is a bag-shaped structure, and in the present embodiment, the blood pressure measuring device 1 has a configuration in which air is used by the pump 14, and thus the air bag will be used for description.
- the bag-shaped structure may be a fluid bag that expands with the fluid.
- the plurality of air bags 81 are laminated and fluidly communicate with each other in the stacking direction.
- the air bag 81 is formed in a rectangular bag shape that is long in one direction. Further, the width of the air bag 81 in the lateral direction is set to be the same as the width of the carla 5 in the lateral direction.
- the air bag 81 is formed by, for example, combining two sheet members 86 and heat-welding them in a rectangular frame shape long in one direction as shown in FIGS. 8, 9, 13 to 17, as shown by the welding portion 81a. It is composed. Further, in the two-layer air bag 81, the two air bags 81 are welded by heat and combined integrally, or the air bags 81 are welded after welding the opposing sheet members 86 of the adjacent air bags 81. It is composed by forming.
- the two-layer air bags 81 are fluidly continuous by openings provided in the sheet members 86 facing each other. Further, in the two-layer air bag 81, the opposing sheet members 86 are bridge-welded to each other in a four-sided frame shape smaller than the welding portion 81a located on the outer peripheral edge, and the bridge welding portion 81b surrounds a plurality of openings. Adjacent air bags 81 are integrally formed and fluidly continuous inside the bridge welded portion 81b.
- the bridge welding and the bridge of the bridge welding portion mean that the adjacent air bags 81 are integrally joined.
- a single or a plurality of jointed portions 82 are provided on at least a part of the edge portion of the air bag 81 arranged adjacent to the carla 5.
- the jointed portion 82 is formed by a part of the sheet member 86 constituting the air bag 81.
- one joint portion 82 is provided on each of the lateral edges of the air bag 81.
- the jointed portion 82 may be divided in the longitudinal direction of the air bag 81 by a slit, or may be provided in plurality in the longitudinal direction of the air bag 81.
- the jointed portion 82 is joined to at least the outer peripheral surface of the carla 5 when the pressing cuff 71 is arranged on the inner peripheral surface of the carla 5.
- the two joints 82 are laminated and welded together.
- the two jointed portions 82 are set to, for example, different lengths in the lateral direction of the air bag 81.
- the two joints 82 are laminated and welded on one end side of the carla 5 in the lateral direction.
- the length of the two jointed portions 82 can be appropriately set as long as the tips can be arranged on the outer peripheral surface of the carla 5, and the two joint portions 82 may or may not be laminated, but can be laminated. When set to a value, it is preferable that the tip does not extend outward from the outer edge of the outer peripheral surface of the carla 5.
- the flow path body 83 is integrally provided at one end of one air bag 81, for example, an air bag 81 adjacent to the carla 5 in the longitudinal direction. Be done.
- the flow path body 83 is provided at the end of the air bag 81 near the device main body 3.
- the flow path body 83 is formed in a width smaller than the width in the lateral direction of the air bag 81 and is formed in a long shape in one direction, and the tip is formed in a circular shape.
- the flow path body 83 has a connecting portion 84 at the tip thereof.
- the flow path body 83 is connected to the flow path portion 15 via the connection portion 84, and constitutes a flow path between the flow path portion 15 of the apparatus main body 3 and the air bag 81.
- a part of the sheet member 86 adjacent to the region constituting the air bag 81 of the sheet member 86 is formed into a long frame shape in one direction. It is composed of welding by heat.
- Such a flow path body 83 is arranged between the inner peripheral surface of the carla 5 and the tension cuff 74, and the tip thereof is the main surface on the wrist 200 side of the region where the cover portion 5a of the carla 5 is provided. , Is arranged at a position facing the first hole portion 5f1.
- the air bag 81 provided with the flow path body 83, a part of the welding portion 81a for welding the two sheet members 86 in a rectangular frame shape is non-welded, and the air bag 81 is continuous with the welding portion 83a constituting the flow path body 83.
- the air bag 81 is fluidly continuous with the flow path body 83.
- connection portion 84 is, for example, a nipple.
- the connecting portion 84 is provided at the tip of the flow path body 83.
- the tip of the connecting portion 84 is exposed from the seat member 86 facing the carla 5 among the two seat members 86 constituting the flow path body 83.
- the connecting portion 84 is inserted into the first hole portion 5f1 of the cover portion 5a and connected to the flow path portion 15.
- the pressing cuff 71 having such a configuration has the first sheet member 86a, the first sheet member 86a, and the first layer of air from the wrist 200 side, as shown in FIGS. 8, 9, and 52.
- the second sheet member 86b constituting the bag 81 and the second sheet member 86b are integrally joined, and the third sheet member 86c forming the bonded portion 82, the third sheet member 86c, and the second layer of air are joined.
- a fourth sheet member 86d constituting the bag 81 and the flow path body 83 is provided.
- the pressing cuff 71 is integrally formed by joining adjacent sheet members 86 by heat welding.
- the first sheet member 86a and the second sheet member 86b are formed in the same rectangular shape as the air bag 81, and the peripheral edges of the four sides are welded to form the air bag 81.
- the second seat member 86b and the third seat member 86c are arranged so as to face each other, and have a plurality of openings 86b1 and 86c1 that fluidly connect the two air bags 81, respectively.
- the second sheet member 86b and the third sheet member 86c are integrally bridge-welded around the plurality of openings 86b1 and 86c1 in a four-sided frame shape smaller than the four sides to which the air bag 81 is welded by heat. Be joined.
- the third sheet member 86c is formed in a shape capable of forming, for example, the air bag 81, the jointed portion 82, and the flow path body 83.
- the fourth sheet member 86d is configured, for example, in a shape capable of forming the air bag 81 and the flow path body 83. Further, the fourth sheet member 86d has, for example, a hole 86d1 into which the tip of the connecting portion 84 can be inserted.
- the third sheet member 86c and the fourth sheet member 86d are arranged so as to face each other, and along the peripheral shape of the air bag 81 and the flow path body 83 so that the air bag 81 and the flow path body 83 are fluidly continuous.
- the air bag 81, the bonded portion 82, and the flow path body 83 are formed by being welded by heat and cut into a predetermined shape.
- connection portion 84 is arranged in the hole portion 86d1 of the fourth sheet member 86d, and the periphery of the hole portion 86d1 is welded to the connection portion 84 by heat. Further, the fourth sheet member 86d is joined to the inner peripheral surface of the carla 5, and the bonded portion 82 of the third sheet member 86c is joined to the outer peripheral surface of the carla 5 via the joining layer 75.
- the back plate 72 is attached to the outer surface of the first sheet member 86a of the pressing cuff 71 by the joining layer 75.
- the back plate 72 is made of a resin material and is formed in a plate shape.
- the back plate 72 is made of polypropylene, for example, and is formed in a plate shape having a thickness of about 1 mm.
- the back plate 72 has shape followability.
- the shape followability means a function in which the back plate 72 can be deformed so as to imitate the shape of the contacted portion of the wrist 200 to be arranged, and the back plate 72 faces the contacted portion of the wrist 200.
- the contact here includes both direct contact and indirect contact via the sensing cuff 73.
- the back plate 72 has a plurality of grooves 72a extending in a direction orthogonal to the longitudinal direction on both main surfaces thereof.
- the plurality of grooves 72a face each other in the thickness direction of the back plate 72. Further, the plurality of grooves 72a are arranged at equal intervals in the longitudinal direction of the back plate 72.
- the back plate 72 Since the portion of the back plate 72 having the plurality of grooves 72a is thinner than the portion having the plurality of grooves 72a, the portion having the plurality of grooves 72a is easily deformed. Therefore, the back plate 72 follows the shape of the wrist 200. It deforms and has a shape-following property that extends in the circumferential direction of the wrist.
- the back plate 72 is formed to have a length that covers the palm side of the wrist 200.
- the back plate 72 transmits the pressing force from the pressing cuff 71 to the main surface of the sensing cuff 73 on the back plate 72 side while following the shape of the wrist 200.
- the sensing cuff 73 is fluidly connected to the pump 14 via the flow path portion 15.
- the sensing cuff 73 is fixed to the main surface of the back plate 72 on the wrist 200 side. As shown in FIGS. 4 and 52, the sensing cuff 73 comes into direct contact, for example, with the region of the wrist 200 where the artery 210 resides.
- the artery 210 is a radial artery and an ulnar artery.
- the sensing cuff 73 is formed in the same shape as the back plate 72 or smaller than the back plate 72 in the longitudinal direction and the width direction of the back plate 72.
- the sensing cuff 73 expands to compress the area of the wrist 200 on the palm side of the artery 210.
- the sensing cuff 73 is pressed toward the wrist 200 side via the back plate 72 by the expanded pressing cuff 71.
- the sensing cuff 73 includes one air bag (second bag-shaped structure) 91 and the air bag 91, as shown in FIGS. 8, 9, 13, 14, 17, and 18. It includes a flow path body 92 that communicates with the flow path body 92, a connecting portion 93 provided at the tip of the flow path body 92, and a joining allowance 94 that is at least partially joined to the pressing cuff 71.
- one main surface of the air bag 91 is fixed to the back plate 72.
- the sensing cuff 73 is joined to the main surface of the back plate 72 on the wrist 200 side by the joining layer 75.
- Such a sensing cuff 73 is configured by integrally welding two sheet members 96.
- the air bag 91 is a bag-shaped structure, and in the present embodiment, the blood pressure measuring device 1 has a configuration in which air is used by the pump 14, and thus the air bag will be used for description.
- the bag-shaped structure may be a liquid bag or the like.
- the air bag 91 is formed in a rectangular shape that is long in one direction.
- the air bag 91 is formed into a rectangular frame that is long in one direction, for example, by combining two sheet members 96 and showing the welded portion 91a in FIGS. 8, 9, 13, 14, 17, and 18. It is composed of welding by heat.
- the flow path body 92 is integrally provided on a part of the edge portion at one end in the longitudinal direction of the air bag 91.
- the flow path body 92 is provided at the end of the air bag 91 near the device main body 3.
- the flow path body 92 is formed in a width smaller than the width in the lateral direction of the air bag 91 and is formed in a long shape in one direction, and the tip is formed in a circular shape.
- the flow path body 92 has a connecting portion 93 at the tip thereof.
- the flow path body 92 has a connecting portion 93 at the tip thereof.
- the flow path body 92 is connected to the flow path portion 15 via the connection portion 93, and constitutes a flow path between the flow path portion 15 of the apparatus main body 3 and the air bag 91.
- a part of the sheet member 96 adjacent to the region constituting the air bag 91 of the sheet member 96 is formed into a long frame shape in one direction. It is composed of welding by heat.
- the air bag 91 has a structure in which a part of the welding portion 91a for welding the two sheet members 96 in a rectangular frame shape is non-welded and is continuous with the welding portion 92a constituting the flow path body 92.
- the air bag 91 and the flow path body 92 are fluidly continuous.
- Such a flow path body 92 is arranged between the inner peripheral surface of the carla 5 and the tension cuff 74, and the tip thereof is the main surface on the wrist 200 side of the region where the cover portion 5a of the carla 5 is provided. , Is arranged at a position facing the second hole portion 5f2.
- connection portion 93 is, for example, a nipple.
- the connecting portion 93 is provided at the tip of the flow path body 92. Further, the tip of the connecting portion 93 is exposed to the outside from the seat member 96 facing the carla 5 and the back plate 72 among the two seat members 96 constituting the flow path body 92.
- the connecting portion 93 is inserted into the second hole portion 5f2 of the cover portion 5a and connected to the flow path portion 15.
- the joining allowance 94 can be joined to the air bag 81 adjacent to the air bag 91 among the plurality of air bags 81 of the pressing cuff 71, in other words, to a part of the welded portion 81a of the air bag 81 on the back plate 72 side by welding. It is formed, and as a specific example, it is joined to an outer edge portion along the longitudinal direction of the air bag 81 on the back plate 72 side.
- the outer edge of the air bag 81 is a region around the outer edge of the air bag 81.
- the air bag 81 is configured by welding two sheet members 86, the welded portion 81a is an example of the outer edge portion of the air bag 81.
- the joining allowance 94 is formed continuously and integrally with, for example, a welded portion 91a of the air bag 91 and a part of the welded portion 92a of the flow path body 92. Therefore, a part of the joint allowance 94 is formed at the outer edge portion along the longitudinal direction of the air bag 91.
- the joining allowance 94 is, for example, a region of the two sheet members 96 that constitutes the air bag 91 and a region that is adjacent to the region that constitutes the flow path body 92, and the air bag 81 on the back plate 72 side of the pressing cuff 71. It is formed by forming the same shape as the welded portion 81a.
- the outer edge portion of the joint allowance 94 is formed to have the same shape as the welded portion 81a of the air bag 81 on the back plate 72 side of the pressing cuff 71.
- the portion facing the welding portion 81a along the longitudinal direction of the air bag 81 constitutes the bonding portion 94a to be welded to the welding portion 81a.
- the joint portion 94a is joined to the pressing cuff 71 by welding.
- the two outer edge portions of the joining allowance 94 along the longitudinal direction of the air bag 91 of the sensing cuff 73 are joined from one end to the other end of the welded portion 81a along the longitudinal direction of the air bag 81.
- the outer edge portion of the joining allowance 94 along the lateral direction is not joined to the welded portion 81a along the lateral direction of the air bag 81.
- the sensing cuff 73 having such a configuration includes a fifth seat member 96a and a sixth seat member 96b from the wrist 200 side, as shown in FIGS. 8 and 9.
- the sensing cuff 73 is configured by joining adjacent sheet members 96 by heat welding.
- the fifth sheet member 96a and the sixth sheet member 96b are configured in a shape capable of forming the air bag 91, the flow path body 92, and the joining allowance 94.
- the fifth sheet member 96a and the sixth sheet member 96b are arranged so as to face each other, and along the peripheral shape of the air bag 91 and the flow path body 92 so that the air bag 91 and the flow path body 92 are fluidly continuous.
- the air bag 91, the flow path body 92, and the bonding allowance 94 are formed by being welded by heat and cut into a predetermined shape.
- the sixth sheet member 96b has, for example, a hole 96b1 into which the tip of the connecting portion 93 can be inserted.
- the connection portion 93 is arranged in the hole portion 96b1, and the periphery of the hole portion 96b1 is welded to the connection portion 93 by heat.
- the sixth sheet member 96b is joined to the inner peripheral surface of the back plate 72 via the joining layer 75.
- the pressing cuff 71 and the sensing cuff 73 are fixed, and the back plate 72 is fixed to the pressing cuff 71 and the sensing cuff 73.
- the cuff unit 250 is manufactured by using a jig 400 having a mounting surface 401 having a curved surface, which will be described later, so that the pressing cuff 71 of the carla 5 is joined in a state before being joined to the carla 5. It is constructed in a curved shape that follows the surface of the surface.
- the tension cuff 74 is fluidly connected to the pump 14 via the flow path portion 15. As shown in FIG. 4, the tension cuff 74 pulls the belt 4 and the carla 5 toward the back side of the wrist 200 by pressing the carla 5 so as to be separated from the wrist 200 by expanding. As shown in FIGS. 10, 11, 20, and 21, the tension cuff 74 includes a plurality of, for example, six-layer air bags 101 and a joint portion 102 provided on the air bag 101 facing the carla 5. , A connecting portion 103 provided in the air bag 101 facing the carla 5, and at least a notch 104 provided in the air bag 101 facing the carla 5. Such a tension cuff 74 is configured by integrally welding a plurality of sheet members 106.
- the tension cuff 74 is fixed to the area where the flow path bodies 83 and 92 are provided and to the back side of the wrist 200 of the carla 5 including the cover portion 5a. That is, the flow path body 83 of the pressing cuff 71 and the flow path body 92 of the sensing cuff 73 are arranged between the back side of the wrist 200 of the carla 5 and the tension cuff 74.
- the tension cuff 74 has the thickness at the time of expansion in the expansion direction, in the present embodiment, in the direction opposite to the carla 5 and the wrist 200, the thickness at the time of expansion of the pressing cuff 71 in the expansion direction, and sensing.
- the cuff 73 is thicker than the thickness at the time of expansion in the expansion direction. That is, the air bag 101 of the tension cuff 74 has a layer structure larger than that of the air bag 81 of the pressing cuff 71 and the air bag 91 of the sensing cuff 73, and the thickness when expanded from the carla 5 toward the wrist 200 is increased. It is thicker than the pressing cuff 71 and the sensing cuff 73.
- the tension cuff 74 including the six-layer air bag 101 is attached to the first outer layer 111 and the first outer layer 111 composed of one air bag 101, as shown in FIGS. 10, 11 and 20.
- a second intermediate layer 113 to be formed and a second outer layer 114 composed of one air bag 101 fused and integrally combined with the second intermediate layer 113 by heat are provided.
- the air bag 101 is a bag-shaped structure, and in the present embodiment, the blood pressure measuring device 1 has a configuration in which air is used by the pump 14, and thus the air bag will be used for description.
- the bag-shaped structure may be a fluid bag that expands with the fluid.
- the plurality of air bags 101 are laminated and fluidly communicate with each other in the stacking direction.
- the air bag 101 is formed in a rectangular bag shape that is long in one direction. Further, the width of the air bag 101 in the lateral direction is set to be the same as the width of the carla 5 in the lateral direction.
- the air bag 101 is formed into a rectangular frame that is long in one direction, for example, by combining two sheet members 106 and showing the welded portion 101a in FIGS. 10, 11, 13, 14, 20, and 21. It is composed of welding by heat.
- the six-layer air bags 101 are fluidly continuous by openings provided in the sheet members 106 facing each other.
- the six-layer air bag 101 is a sheet in which the first outer layer 111 and the first intermediate layer 112, the first intermediate layer 112 and the second intermediate layer 113, and the second intermediate layer 113 and the second outer layer 114 face each other.
- the members 106 are bridge-welded to each other in a four-sided frame shape smaller than the welding portion 81a located on the outer peripheral edge, and the bridge welding portions 101b surround a plurality of openings to integrally form adjacent air bags 101. It is fluidly continuous inside the bridge welding portion 101b.
- the first outer layer 111 is formed by one air bag 101 arranged on the wrist 200 side.
- the first outer layer 111 constitutes the first layer air bag 101 from the wrist 200 side of the six layers air bag 101.
- the first intermediate layer 112 is laminated on the first outer layer 111.
- the first intermediate layer 112 is formed by a two-layer air bag 101.
- the first intermediate layer 112 constitutes the second layer and the third layer air bag 101 from the wrist 200 side among the six layers of air bag 101.
- the first intermediate layer 112 is configured by integrally welding two layers of air bags 101 at the outer peripheral edge. In other words, the first intermediate layer 112 is formed by integrally welding four sheet members 106 in the shape of the outer peripheral edge of the air bag 101.
- the second intermediate layer 113 is laminated on the first intermediate layer 112.
- the second intermediate layer 113 is formed by a two-layer air bag 101.
- the second intermediate layer 113 constitutes the fourth layer and the fifth layer of the air bag 101 from the wrist 200 side among the six layers of the air bag 101.
- the second intermediate layer 113 is formed by integrally welding the two layers of air bags 101 at the outer peripheral edge. In other words, the second intermediate layer 113 is formed by integrally welding the four sheet members 106 in the shape of the outer peripheral edge of the air bag 101.
- the second outer layer 114 is formed by one air bag 101 arranged on the carla 5 side.
- the second outer layer 114 constitutes the sixth layer air bag 101 from the wrist 200 side of the six layers air bag 101.
- a single or a plurality of jointed portions 102 are provided on at least a part of the edge portion of the air bag 101 arranged adjacent to the carla 5.
- the jointed portion 102 is formed by a part of the sheet member 106 constituting the air bag 101.
- jointed portions 102 will be provided on each of the lateral edges of the air bag 101 in the longitudinal direction of the air bag 101.
- the jointed portion 102 is provided in the air bag 101 while avoiding a position facing the cover portion 5a of the carla 5.
- the jointed portion 102 has a relief portion 102a for exposing the feeding terminal 8b to the outside at a portion of the feeding portion 8 provided on the carla 5 facing the feeding terminal 8b described later.
- the relief portion 102a is, for example, an opening capable of exposing the power feeding terminal 8b to the outside, and has a circular shape as an example.
- the jointed portion 102 is joined to at least the outer peripheral surface of the carla 5 when the tension cuff 74 is arranged on the inner peripheral surface of the carla 5. Further, the jointed portions 102 arranged at the same position in the lateral direction of the air bag 101 are laminated and welded.
- the two jointed portions 102 are set to, for example, different lengths in the lateral direction of the air bag 101.
- the two joints 102 are laminated and welded on one end side of the carla 5 in the lateral direction.
- the length of the two bonded portions 102 can be appropriately set as long as the tips can be arranged on the outer peripheral surface of the carla 5, and the two joint portions 102 may or may not be laminated, but can be laminated. When set to a value, it is preferable that the tip does not extend outward from the outer edge of the outer peripheral surface of the carla 5.
- connection portion 103 is, for example, a nipple.
- the connecting portion 103 is provided at a position on the central side in the longitudinal direction of the air bag 101 arranged adjacent to the carla 5 and facing the third hole portion 5f3 of the cover portion 5a.
- the tip of the connecting portion 103 is exposed from the seat member 106 facing the carla 5 among the two seat members 106 constituting the air bag 101.
- the connecting portion 103 is inserted into the third hole portion 5f3 of the cover portion 5a and connected to the flow path portion 15.
- the notch portion 104 is provided at a position facing the relief portion 5b provided on the carla 5.
- the cutout portion 104 is provided in the air bag 101 of the sixth layer forming the second outer layer 114.
- the tension cuff 74 has a seventh seat member 106a, an eighth seat member 106b, a ninth seat member 106c, and a tenth seat member 106c from the wrist 200 side.
- Sheet member 106d, 11th sheet member 106e, 12th sheet member 106f, 13th sheet member 106g, 14th sheet member 106h, 15th sheet member 106i, 16th sheet member 106j, 17th sheet A member 106k and an 18th sheet member 106l are provided.
- the tension cuff 74 is integrally formed by joining adjacent sheet members 106 by heat welding.
- the 7th sheet member 106a to the 18th sheet member 106l are formed in the same rectangular shape as the air bag 101.
- the seventh sheet member 106a and the eighth sheet member 106b are welded by heat along the shape of the peripheral edges of the four sides of the air bag 101 to form the first air bag 101 from the wrist 200 side. That is, the 7th sheet member 106a and the 8th sheet member 106b form the first outer layer 111.
- the eighth sheet member 106b and the ninth sheet member 106c are arranged so as to face each other, and have a plurality of openings 106b1 and 106c1 that fluidly connect the two air bags 101, respectively. Further, the eighth sheet member 106b and the ninth sheet member 106c are integrally bridge-welded around the plurality of openings 106b1 and 106c1 in a four-sided frame shape smaller than the four sides to which the air bag 101 is welded by heat. Be joined.
- the 9th sheet member 106c and the 10th sheet member 106d are welded by heat along the shape of the peripheral edges of the four sides of the air bag 101 to form the second layer air bag 101 from the wrist 200 side.
- the tenth sheet member 106d and the eleventh sheet member 106e are arranged to face each other as shown in FIGS. 10 and 11 and 20, respectively, and a plurality of openings 106d1 that fluidly connect the two air bags 101. It has 106e1.
- the eleventh sheet member 106e and the twelfth sheet member 106f are welded by heat along the shape of the peripheral edges of the four sides of the air bag 101 to form the third layer air bag 101 from the wrist 200 side.
- the ninth sheet member 106c, the tenth sheet member 106d, the eleventh sheet member 106e, and the twelfth sheet member 106f are integrally welded by heat along the shape of the peripheral edges of the four sides of the air bag 101.
- the first intermediate layer 112 in which the air bags 101 of the second layer and the third layer are integrally formed is formed.
- the twelfth sheet member 106f and the thirteenth sheet member 106g are arranged to face each other, and a plurality of openings 106f1 that fluidly connect the two air bags 101, respectively. It has 106 g1. Further, the 12th sheet member 106f and the 13th sheet member 106g are integrally bridge-welded around the plurality of openings 106f1 and 106g1 in a four-sided frame shape smaller than the four sides on which the air bag 101 is welded by heat. Be joined.
- the 13th sheet member 106g and the 14th sheet member 106h are welded by heat along the shape of the peripheral edges of the four sides of the air bag 101 to form the fourth layer air bag 101 from the wrist 200 side.
- the 14th sheet member 106h and the 15th sheet member 106i are arranged to face each other as shown in FIGS. 10, 11 and 21, respectively, and a plurality of openings 106h1 that fluidly connect the two air bags 101, respectively. It has 106i1.
- the 15th sheet member 106i and the 16th sheet member 106j are welded by heat along the shape of the peripheral edges of the four sides of the air bag 101 to form the fifth layer air bag 101 from the wrist 200 side.
- the 13th sheet member 106g, the 14th sheet member 106h, the 15th sheet member 106i, and the 16th sheet member 106j are integrally welded by heat along the peripheral edges of the four sides of the air bag 101.
- the second intermediate layer 113 is formed by integrally forming the air bags 101 of the fourth layer and the fifth layer.
- the 16th sheet member 106j and the 17th sheet member 106k are arranged so as to face each other, and a plurality of openings 106j1 that fluidly connect the two air bags 101, respectively. It has 106k1. Further, the 17th sheet member 106k is formed in a shape capable of forming, for example, the air bag 101 and the jointed portion 102. The 16th sheet member 106j and the 17th sheet member 106k are integrally joined by heat-bridge welding around the plurality of openings 106j1 and 106k1 in a four-sided frame shape smaller than the four sides on which the air bag 101 is welded. To.
- the 17th sheet member 106k and the 18th sheet member 106l are welded by heat along the shape of the peripheral edges of the four sides of the air bag 101 and cut into a predetermined shape to form a notch in the sixth layer from the wrist 200 side. It constitutes an air bag 101 having 104 and a joint portion 102.
- the 18th sheet member 106l has, for example, a hole 106l1 into which the tip of the connecting portion 103 can be inserted.
- the connecting portion 103 is arranged in the hole portion 106l1, and the periphery of the hole portion 106l1 is heat-welded to the connecting portion 103.
- the 18th sheet member 106l is bonded to the inner peripheral surface of the carla 5, and the bonded portion 102 of the 17th sheet member 106k is bonded to the outer peripheral surface of the carla 5 via the bonding layer 75.
- each sheet member 86, 96, 106 forming the pressing cuff 71, the sensing cuff 73, and the tension cuff 74 are formed to have a thickness of, for example, 0.15 mm.
- Each sheet member 86, 96, 106 is formed of a thermoplastic resin material.
- the thermoplastic resin material is a thermoplastic elastomer.
- Examples of the thermoplastic resin material constituting the sheet members 86, 96, 106 include a thermoplastic polyurethane resin (Thermoplastic PolyUrethane, hereinafter referred to as TPU), a vinyl chloride resin (PolyVinyl Chloride), and an ethylene vinyl acetate resin (Ethylene-).
- thermoplastic Polystyrene-based resin (ThermoplasticPolyStyrene), thermoplastic polyolefin resin (ThermoplasticPolyOlefin), thermoplastic polyester-based resin (ThermoPlasticPolyester), and thermoplastic polyamide resin (ThermoplasticPolyAmide)
- the pressing cuff 71 and the sensing cuff 73 are composed of at least the seat members 86 and 106 welded to the carla 5 among the plurality of seat members 86 and 106 constituting the air bags 81 and 101, which are made of the same material as the carla 5. Will be done.
- the sheet members 86, 96, 106 For example, for the sheet members 86, 96, 106 a molding method such as T-die extrusion molding or injection molding is used. The sheet members 86, 96, 106 are molded by each molding method, then sized into a predetermined shape, and the sized pieces are joined by welding or the like to form a bag-shaped structure 81, 91, 101. To do. High-frequency welder or laser welding is used as the welding method.
- the fluid circuit 7 is composed of a case 11, a pump 14, a flow path portion 15, an on-off valve 16, a pressure sensor 17, a pressing cuff 71, a sensing cuff 73, and a tension cuff 74.
- a specific example of the fluid circuit 7 will be described.
- the fluid circuit 7 has, for example, a first flow path 7a that connects the pump 14, the sensing cuff 73, the first pressure sensor 17A, and the second pressure sensor 17B via the first on-off valve 16A.
- It is configured to be branched from the first flow path 7a between the pump 14 and the first on-off valve 16A, and is sequentially connected to the pump 14 via the second on-off valve 16B, the third on-off valve 16C and the fourth on-off valve 16D.
- It is composed of a second flow path 7b that is continuous with the atmosphere and an intermediate portion between the second on-off valve 16B and the third on-off valve 16C of the second flow path 7b, and the tension cuff 74 is continuously connected from the pump 14.
- the third flow path 7c and the middle part between the third on-off valve 16C and the fourth on-off valve 16D of the second flow path 7b are branched, and the pressing cuff 71 is continuously connected from the pump 14 to the fourth flow. It has a road 7d and.
- the second on-off valve 16B and the third on-off valve 16C are opened, and the first on-off valve 16A and the fourth on-off valve 16D are closed, so that the third flow path branches from the second flow path 7b.
- the 7c and the fourth flow path 7d are connected to the pump 14, and the pump 14, the pressing cuff 71 and the tension cuff are fluidly connected.
- the fluid circuit 7 branches from the first flow path 7a and the second flow path 7b when the first on-off valve 16A, the second on-off valve 16B, and the third on-off valve 16C are opened and the fourth on-off valve 16D is closed.
- the third flow path 7c and the fourth flow path 7d are connected to the pump 14, and the pump 14, the pressing cuff 71 and the tension cuff, and the pump 14 and the sensing cuff 73 are fluidly connected.
- the second on-off valve 16B, the third on-off valve 16C, and the fourth on-off valve 16D are opened, and the first on-off valve 16A is closed, so that the second flow path 7b, the third flow path 7c, and the first on-off valve 7c are closed.
- the four flow paths 7d are connected to the pump 14, and the pump 14, the pressing cuff 71, the tension cuff 74, and the atmosphere are fluidly connected. Further, in the fluid circuit 7, the first on-off valve 16A, the second on-off valve 16B, the third on-off valve 16C, and the fourth on-off valve 16D are opened to open the first flow path 7a, the second flow path 7b, and the third flow.
- the path 7c and the fourth flow path 7d are connected to the pump 14, and the pump 14, the pressing cuff 71, the sensing cuff 73, the tension cuff 74, and the atmosphere are fluidly connected.
- the power feeding unit 8 is provided in the recess 5c formed on the outer surface of the carla 5 protruding from the device main body 3 on one end side.
- the power feeding unit 8 is configured to be connectable to a connector provided on the charging cable of the charger.
- the power supply unit 8 includes a wiring unit 8a, a power supply terminal 8b, and a cover 8c that covers the wiring unit 8a arranged in the recess 5c of the carla 5. .. One end of the wiring unit 8a is connected to the power feeding terminal 8b, and the other end is connected to the control unit 55.
- the power supply terminal 8b is composed of, for example, two circular terminals.
- the wiring portion 8a and the power feeding terminal 8b are formed of FPC (Flexible printed circuits) or the like in which a conductive metal film or the like is provided on a base film such as polyimide.
- the cover 8c is formed to have the same shape as the recess 5c, covers the recess 5c, and when provided in the recess 5c, the upper surface is flush with the outer surface on the short side of the carla 5.
- a first structure 251 is formed by welding and integrating a plurality of sheets constituting the pressing cuff 71.
- the material is cut (step ST11) to form a sheet having a predetermined shape.
- the predetermined shape is a shape including, in addition to the shape of the air bag 81 and the jointed portion 82, a welding allowance, a dummy portion for alignment for aligning with each processing machine, and the like.
- the first sheet 86A, the second sheet 86B, the third sheet 86C, and the fourth sheet Punch out each 86D are shown in FIGS. 23 to 26.
- the first sheet 86A is a rectangular sheet member having a positioning pin hole 71a into which the positioning pin 301 can be inserted and which is larger than the outer peripheral edge shape of the air bag 81.
- the first sheet 86A forms the first sheet member 86a.
- a plurality of pin holes 71a are formed, as a specific example.
- the two pin holes 71a are arranged one on each side in the longitudinal direction of the air bag 81 so as to sandwich the region constituting the air bag 81 of the first sheet 86A.
- the second sheet 86B has a positioning pin hole 71a into which the positioning pin 301 can be inserted, and an opening for fluidly communicating the adjacent air bag 81, and the outer peripheral edge of the air bag 81. It is a rectangular sheet member larger than the shape.
- the second sheet 86B forms the second sheet member 86b.
- a plurality of pin holes 71a are formed, as a specific example.
- One pin hole 71a is arranged on each side of the second sheet 86B in the longitudinal direction of the air bag 81 so as to sandwich the region constituting the air bag 81. Further, here, the opening of the second sheet 86B constitutes the opening 86b1 of the second sheet member 86b.
- the third sheet 86C has a positioning pin hole 71a into which the positioning pin 301 can be inserted, and an opening for fluidly communicating the adjacent air bag 81, and is joined to the air bag 81. It is a rectangular sheet member larger than the outer peripheral edge shape of the portion 82.
- the third sheet 86C forms the third sheet member 86c.
- a plurality of pin holes 71a are formed, as a specific example.
- One pin hole 71a is arranged on each side of the third sheet 86C in the longitudinal direction of the air bag 81 so as to sandwich the region constituting the air bag 81.
- the opening of the third sheet 86C constitutes the opening 86c1 of the third sheet member 86c.
- the fourth sheet 86D has a positioning pin hole 71a into which the positioning pin 301 can be inserted, and a hole 86d1 into which the connecting portion 84 is inserted, and has a rectangle larger than the outer peripheral shape of the air bag 81 and the jointed portion 82. It is a sheet member with a shape.
- the fourth sheet 86D forms the fourth sheet member 86d.
- a plurality of pin holes 71a are formed, as a specific example.
- One pin hole 71a is arranged on each side of the fourth sheet 86D in the longitudinal direction of the air bag 81 so as to sandwich the region constituting the air bag 81.
- the connecting portion 84 is welded to the fourth sheet 86D (step ST12).
- the connecting portion 84 is inserted into the hole portion 86d1 provided in the fourth sheet 86D, and the connecting portion 84 is welded to the fourth sheet 86D by a high frequency welding machine.
- the second sheet 86B and the third sheet 86C are bridge welded (step ST13). Specifically, the second sheet 86B and the third sheet 86C are laminated, and the positioning pin holes 71a of the second sheet 86B and the third sheet 86C are arranged in the positioning pin 301, and the lower mold 302 is used for the first. The second sheet 86B and the third sheet 86C are arranged. As a result, the sheets 86B and 86C are positioned with respect to the lower mold 302.
- the lower mold 302 is provided with an electrode portion 302a which is a protrusion constituting the electrode.
- the electrode portion 302a is formed in a shape capable of contacting the region where the second sheet 86B and the third sheet 86C are welded, and the electrode portion 302a used in this step has an end face having a bridge welding portion 81b. It is a protrusion formed on.
- the bridge is welded in a rectangular frame shape smaller than the outer peripheral edge shape of the air bag 81 by a high-frequency welding machine to form the bridge welding portion 81b, and the second sheet 86B and the third sheet 86C are integrally welded.
- the first sheet 86A is welded to the second sheet 86B.
- the positioning pin holes 71a of the second sheet 86B and the third sheet 86C and the first sheet 86A that were bridge-welded in step ST13 were arranged in the positioning pin 301 and bridge-welded to the lower mold 302.
- the second sheet 86B, the third sheet 86C, and the first sheet 86A are arranged.
- the electrode portion 302a of the lower mold 302 used in this step is a protrusion whose end face is formed in the shape of the welded portion 81a.
- the second sheet 86B, the third sheet 86C, the first sheet 86A, and the fourth sheet 86D which are integrated by welding, are welded.
- the respective positioning pins of the second sheet 86B, the third sheet 86C, the first sheet 86A, and the fourth sheet 86D integrated by welding are arranged.
- the hole 71a is arranged in the positioning pin 301, and the second sheet 86B, the third sheet 86C, the first sheet 86A, and the fourth sheet 86D integrated with the lower mold 302 by welding are arranged.
- the second sheet 86B, the third sheet 86C, and the first sheet 86A integrated by welding are the second sheet 86B and the first sheet 86A integrated by bridge welding as shown in FIGS. 27 and 28.
- the three sheets 86C and the first sheet 86A welded at the welding portion 81a as shown in FIGS. 29 and 30.
- the electrode portion 302a of the lower mold 302 used in this step is a protrusion whose end faces are formed in the shape of the welded portion 81a and the welded portion 83a. That is, the shape of the end surface of the electrode portion 302a is a shape that can form the air bag 81 and the flow path body 83.
- the cavity 302b provided in the lower mold 302 faces the portion where at least the third sheet 86C and the fourth sheet 86D of the first sheet 86A and the second sheet 86B are welded. Let the part escape. Then, it is welded to the outer peripheral edge shape of the air bag 81 and the outer peripheral edge shape of the flow path body 83 by a high-frequency welding machine to form the welded portion 81a and the welded portion 83a. By these steps, the first structure 251 is manufactured.
- a second structure 252 which is a part of the cuff unit 250, is formed by welding and integrating a plurality of sheets constituting the sensing cuff 73.
- the second structure 252 is manufactured after the first structure 251 is manufactured will be described, but the first structure 251 and the second structure 252 are manufactured.
- the order is not limited.
- the first structure 251 and the second structure 252 may be manufactured in parallel.
- the material is cut (step ST21) to form a sheet having a predetermined shape.
- the predetermined shape is a shape including a welding allowance, a dummy portion for alignment for aligning with each processing machine, and the like, in addition to the shape of the air bag 91 and the flow path body 92.
- the fifth sheet 96A and the sixth sheet 96B are punched out from the sheet-like material formed of the thermoplastic resin material by a press machine, respectively.
- the fifth sheet 96A is a rectangular sheet member having a positioning pin hole 73a into which the positioning pin 321 can be inserted and which is larger than the outer peripheral edge shape of the air bag 91 and the flow path body 92. is there.
- the fifth sheet 96A forms the fifth sheet member 96a.
- a plurality of pin holes 73a are formed, as a specific example.
- the two pin holes 73a are arranged one on each side in the longitudinal direction of the air bag 91 so as to sandwich the region constituting the air bag 91 of the fifth sheet 96A.
- the sixth sheet 96B has a positioning pin hole 73a into which the positioning pin 321 can be inserted and a hole 96b1 into which the connecting portion 93 is inserted, and is formed of the air bag 91 and the flow path body 92. It is a rectangular sheet member larger than the outer peripheral shape.
- the sixth sheet 96B forms the sixth sheet member 96b.
- a plurality of pin holes 73a are formed, as a specific example.
- the two pin holes 73a are arranged one on each side in the longitudinal direction of the air bag 91 so as to sandwich the region constituting the air bag 91 of the sixth sheet 96B.
- the connecting portion 93 is welded to the sixth sheet 96B (step ST22).
- the connecting portion 93 is inserted into the hole portion 96b1 provided in the sixth sheet 96B, and the connecting portion 93 is welded to the sixth sheet 96B by a high frequency welding machine.
- the fifth sheet 96A and the sixth sheet 96B are welded.
- the positioning pin holes 73a of the fifth sheet 96A and the sixth sheet 96B are arranged in the positioning pin 321, and the fifth sheet 96A and the sixth sheet 96B are arranged in the lower mold 320.
- the fifth sheet 96A and the sixth sheet 96B are positioned with respect to the lower mold 320.
- the electrode portion 322 of the lower mold 320 used in this step is a protrusion whose end face is formed in the shape of the welded portion 91a of the air bag 91 and the welded portion 92a of the flow path body 92.
- it is welded to the outer peripheral shape of the air bag 91 and the outer peripheral shape of the flow path body 92 by a high-frequency welding machine to form the welded portions 81a and 91a.
- the second structure 252 is manufactured by these steps.
- the first fixing is performed (step ST31).
- the first structure 251 and the back plate 72 are fixed.
- the back plate 72 is placed on a curved jig and heat-processed by heating in a heating furnace to bend it into a predetermined shape.
- the predetermined shape referred to here is a shape along the surface of the carla 5 with which the back plate 72 faces with the pressing cuff 71.
- the first structure 251 is set in the jig 400.
- the jig 400 has a mounting surface 401 and a positioning pin 402 for positioning.
- the mounting surface 401 is formed on the curved surface of the carla 5 corresponding to the surface on which the pressing cuff 71 is arranged.
- the mounting surface 401 has at least a size capable of arranging the entire area of the air bag 81 and the entire area of the air bag 91.
- “arrangeable” means that it is arranged at a position overlapping the mounting surface 401 in a plan view. That is, it can be curved along the mounting surface 401 by directly contacting the mounting surface 401, and in the second structure 252, either directly or indirectly through at least one of the first structure 251 and the back plate 72. It is arranged at a position where it can be bent along the mounting surface 401 by coming into contact with the mounting surface 401.
- the mounting surface 401 can arrange the entire area of the air bag 81 and a part of the flow path body 83. Moreover, the entire area of the air bag 91 and a part of the flow path body 92 have a size that can be arranged.
- the curved surface of the carla 5 corresponding to the surface on which the pressing cuff 71 is arranged means that when the cuff unit 250 formed along the curved surface is fixed to the carla 5, the cuff unit 250 becomes the carla 5. It is a curved surface that can suppress the occurrence of wrinkles that inhibit expansion on at least one of the pressing cuff 71 and the sensing cuff 73 by being curved as compared with that before fixing.
- the mounting surface 401 is, for example, a curved surface of the carla 5 having the same curvature as the surface on which the pressing cuff 71 is arranged. In another example, the mounting surface 401 is a curved surface of the carla 5 having substantially the same curvature as the surface on which the pressing cuff 71 is arranged.
- a plurality of positioning pins 402 for positioning are formed, as a specific example, two.
- the positioning pin 402 is configured to be dispositionable in the pin holes 71a of the first structure 251 and the pin holes 73a of the second structure 252.
- the positioning pin 402 for positioning is formed in a shape capable of preventing the movement of the first structure 251 and the second structure 252 with respect to the jig 400, and as a specific example, a shape that fits into the pin holes 71a and 73a.
- One of the positioning pins 402 is arranged at, for example, one end of the mounting surface 401.
- the other pin 402 is arranged at, for example, the other end of the mounting surface 401.
- the first structure 251 is set on the positioning pin 402 for positioning.
- one positioning pin 402 is arranged in one pin hole 71a of the first structure 251 and the other positioning pin 402 is arranged in the other pin hole 71a.
- the one pin hole 71a referred to here is one of the two pin holes 71a of the sheets 86A, 86B, 86C, and 86D, which are arranged opposite to each other.
- the other pin hole 71a is the other pin hole 71a that is arranged to face each other.
- a double-sided tape is attached to the surface of the air bag 81 on the opposite side of the mounting surface 401 of the first structure 251 to form the bonding layer 75.
- the back plate 72 is fixed to the joint layer 75.
- step ST32 perform the second fixing (step ST32).
- the second structure 252 is fixed to the back plate 72.
- a double-sided tape is attached to the surface of the back plate 72 to form the bonding layer 75.
- the second structure 252 is set on the positioning pin 402 for positioning.
- one positioning pin 402 is arranged in one pin hole 73a of the second structure 252, and the other positioning pin 402 is arranged in the other pin hole 73a.
- the one pin hole 73a referred to here is one of the two pin holes 73a of the sheets 96A and 96B, which are arranged opposite to each other.
- the other pin hole 73a is the other pin hole 71a arranged to face each other.
- the second structure 252 is fixed to the back plate 72 by pressing the second structure 252 against the back plate 72.
- the joining allowance 94 of the first structure 251 is joined to the second structure 252 (step ST33).
- the outer edges of the joint allowance 94 two edges along the longitudinal direction of the air bag 91 and along the longitudinal direction of the welded portion 81a of the air bag 81 on the back plate 72 side of the second structure 252.
- the joint portion 94a is formed by welding the two edges with a high-frequency welding machine.
- step ST34 by cutting the integrated first structure 251 and back plate 72, and the second structure 252, the shape of the pressing cuff 71 and the shape of the sensing cuff 73 are formed (step ST34). Cutting is done by, for example, a press or scissors.
- the cuff unit 250 is manufactured by these steps. Next, information such as a lot number is printed at a predetermined position of the manufactured cuff unit 250 (step ST35).
- the cuff unit 250 configured in this way has the first structure 251 and the second structure 252 on the mounting surface 401 formed on the curved surface of the carla 5 corresponding to the surface on which the pressing cuff 71 is fixed. By being welded, the carla 5 is formed into a curved shape that follows the inner peripheral surface to which the pressing cuff 71 is fixed.
- the material is cut (step ST41) to form a sheet member 106 having a predetermined shape.
- the predetermined shape is a shape including, in addition to the shape of the air bag 101 and the jointed portion 102, a welding allowance, a dummy portion for alignment for aligning with each processing machine, and the like.
- the 7th sheet member 106a, the 8th sheet member 106b, the 9th sheet member 106c, the 10th sheet member 106d, and the 11th sheet member The 106e, the 12th sheet member 106f, the 13th sheet member 106g, the 14th sheet member 106h, the 15th sheet member 106i, the 16th sheet member 106j, the 17th sheet member 106k, and the 18th sheet member 106l are punched out, respectively.
- the connecting portion 103 is welded to the 18th sheet member 106l (step ST42).
- the connecting portion 103 is inserted into the hole portion 106l1 provided on the center side of the 18th sheet member 106l, and the connecting portion 103 is welded to the 18th sheet 106l by a high frequency welding machine.
- bridge welding is performed (step ST43).
- the eighth sheet member 106b and the ninth sheet member 106c are sequentially set on the positioning pin of the jig, and the ninth sheet member 106c is placed on the eighth sheet member 106b in an overlapping manner.
- the bridge welding portion 101b is formed by welding in a rectangular frame shape by a high-frequency welding machine so as to surround the openings 106b1 and 106c1 of the sheet members 106b and 106c, and the sheet members 106b and 106c are integrally welded.
- the 12th sheet member 106f and the 13th sheet member 106g are sequentially set on the positioning pin of the jig, and the 13th sheet member 106g is placed on the 12th sheet member 106f in an overlapping manner.
- the bridge welding portion 101b is formed by welding in a rectangular frame shape with a high-frequency welding machine so as to surround the openings 106g1 and 106f1 of the sheet members 106g and 106f, and the sheet members 106g and 106f are integrally welded.
- the 16th sheet member 106j and the 17th sheet member 106k are sequentially set on the positioning pin of the jig, and the 17th sheet member 106k is placed on the 16th sheet member 106j in an overlapping manner.
- the bridge welding portion 101b is formed by welding in a rectangular frame shape with a high-frequency welding machine so as to surround the openings 106j1 and 106k1 of the sheet members 106j and 106k, and the sheet members 106j and 106k are integrally welded.
- the first outer layer 111 is formed (step ST44). Specifically, the eighth sheet member 106b and the ninth sheet member 106c, which were bridge-welded in step ST43, and the seventh sheet member 106a are sequentially set on the positioning pin of the jig, and the outside of the air bag 101 is removed by a high-frequency welding machine. It is welded to the peripheral shape to form the welded portion 101a. As a result, the first outer layer 111 is formed.
- the second outer layer 114 is formed (step ST45). Specifically, the 16th sheet member 106j and the 17th sheet member 106k bridge-welded in step ST33 and the 18th sheet member 106l to which the connecting portion 103 is welded in step ST42 are sequentially set on the positioning pin of the jig. A high-frequency welding machine is used to weld the air bag 101 to the outer peripheral edge shape to form the welded portion 101a. As a result, the second outer layer 114 is formed.
- the jointed portion 102 is formed on the formed second outer layer 114 (step ST46).
- the second outer layer 114 is set on the positioning pin of the jig, and the press mold having a shape that can be cut into the outer peripheral shape of the air bag 101, the joint portion 102, and the notch portion 104 of the sixth layer is formed in step ST45.
- the formed second outer layer 114 is arranged.
- the second outer layer 114 is outside the air bag 101, the jointed portion 102, and the cutout portion 104 of the sixth layer. It is cut into a peripheral shape, and a bonded portion 102 is formed on the second outer layer 114.
- the first intermediate layer 112 and the second intermediate layer 113 are formed (step ST47).
- an intermediate electrode is arranged on the positioning pin of the jig between the 12th sheet member 106f and the 13th sheet member 106g bridge-welded in step ST43.
- the second outer layer 114, the sheet members 106h and 106i without bridge welding, the sheet members 106g and 106f with the intermediate electrodes arranged between them, the sheet members 106d and 106e without bridge welding, and the first outer layer 111 are formed.
- the layers are sequentially laminated and welded to the outer peripheral edge shape of the air bag 101 by a high-frequency welding machine to form the welded portion 101a.
- the first intermediate layer 112 and the second intermediate layer 113 are formed. That is, a six-layer air bag 101 of the first outer layer 111, the first intermediate layer 112, the second intermediate layer 113, and the second outer layer 114 is formed.
- step ST48 the formed first outer layer 111, first intermediate layer 112, and second intermediate layer 113 are finished and cut.
- the tension cuff 74 is manufactured.
- information such as a lot number is printed at a predetermined position on the manufactured tension cuff 74 (step ST49).
- the power feeding unit 8 is formed on the carla 5 (step ST51).
- the FPC constituting the wiring portion 8a and the power supply terminal 8b is joined to the carla 5 with double-sided tape or the like to the cover portion 5a and the recess 5c of the carla 5, and the cover 8c is joined to the recess 5c with double-sided tape or the like.
- the cuff structure 6 is joined to the carla 5 (step ST52).
- a double-sided tape which is a bonding layer 75, is attached to a region of the pressing cuff 71 of the cuff unit 250 facing the carla 5 of the fourth sheet member 86d and the jointed portion 82, and pressed against the carla 5.
- the back plate 72 and the sensing cuff 73 are also attached to the carla 5 at the same time.
- the connecting portion 84 of the pressing cuff 71 and the connecting portion 93 of the sensing cuff 73 are inserted into the first hole portion 5f1 and the second hole portion 5f2 of the cover portion 5a of the carla 5.
- a double-sided tape is attached to the region of the tension cuff 74 facing the carla 5 of the 18th sheet member 106l and the jointed portion 102, and the flow of the pressing cuff 71 arranged on the inner surface of the carla 5 and the carla 5.
- the tension cuff 74 is attached to the flow path body 92 of the road body 83 and the sensing cuff 73. By these steps, the cuff structure 6 is joined to the carla 5.
- step ST53 the seal member 36 and the back cover 35 are arranged on the cover portion 5a, and the back cover 35 is fixed to the cover portion 5a by the first fastening member 35a (step ST53) to form the back cover.
- step ST54 the device main body 3 excluding the back cover 35 is integrally assembled.
- step ST55 the back cover 35 is arranged at the end of the outer case 31 of the apparatus main body 3 on the wrist 200 side, and the outer case 31 and the back cover 35 are fixed by the second fastening member 35b (step ST55).
- step ST56 the first belt 61 and the second belt 62 are assembled in the outer case 31 (step ST56).
- the blood pressure measuring device 1 is manufactured by these steps.
- FIG. 46 is a flow chart showing an example of blood pressure measurement using the blood pressure measuring device 1, and shows both the operation of the user and the operation of the control unit 55.
- FIGS. 47 to 49 show an example in which the user wears the blood pressure measuring device 1 on the wrist 200.
- the user attaches the blood pressure measuring device 1 to the wrist 200 (step ST61).
- the user inserts one of the wrists 200 into the carla 5 as shown in FIG. 47.
- the sensing cuff 73 is arranged in the region where the artery 210 on the palm side of the wrist 200 exists.
- the device body 3 and the tension cuff 74 are arranged on the back side of the wrist 200.
- the second belt 62 is passed through the frame-shaped body 61e of the buckle 61b of the first belt 61 by the hand opposite to the hand on which the user placed the blood pressure measuring device 1.
- the user pulls the second belt 62, brings the member on the inner peripheral surface side of the carla 5, that is, the cuff structure 6 into close contact with the wrist 200, and inserts the rod 61f attached to the small hole 62a.
- the first belt 61 and the second belt 62 are connected, and the blood pressure measuring device 1 is attached to the wrist 200.
- the user operates the operation unit 13 to input a command corresponding to the start of measurement of the blood pressure value.
- the operation unit 13 in which the command input operation is performed outputs an electric signal corresponding to the start of measurement to the control unit 55 (step ST62).
- the control unit 55 opens, for example, the first on-off valve 16A, the second on-off valve 16B, and the third on-off valve 16C, closes the fourth on-off valve 16D, drives the pump 14, and causes the pump 14.
- Compressed air is supplied to the pressing cuff 71, the sensing cuff 73, and the tension cuff 74 via the first flow path 7a, the second flow path 7b, the third flow path 7c, and the fourth flow path 7d (step ST63).
- the pressing cuff 71, the sensing cuff 73 and the tension cuff 74 start expanding.
- the first pressure sensor 17A and the second pressure sensor 17B detect the pressures of the pressing cuff 71, the sensing cuff 73, and the tension cuff 74, and output an electric signal corresponding to these pressures to the control unit 55 (step ST64). Based on the received electric signal, the control unit 55 determines whether or not the pressure in the internal space of the pressing cuff 71, the sensing cuff 73, and the tension cuff 74 has reached a predetermined pressure for blood pressure measurement (step ST65). ).
- the control unit 55 presses the first on-off valve 16A. Closed, compressed air is supplied via the second flow path 7b, the third flow path 7c, and the fourth flow path 7d.
- the control unit 55 stops driving the pump 14 (YES in step ST65). At this time, as shown by the alternate long and short dash line in FIG. 4, the pressing cuff 71 and the tension cuff 74 are sufficiently expanded, and the expanded pressing cuff 71 presses the back plate 72.
- the tension cuff 74 presses the carla 5 in the direction away from the wrist 200
- the belt 4, the carla 5 and the device main body 3 move in the direction away from the wrist 200, and as a result, the pressing cuff 71, The back plate 72 and the sensing cuff 73 are pulled toward the wrist 200 side.
- the belt 4, the carla 5, and the device body 3 move away from the wrist 200 due to the expansion of the tension cuff 74, the belt 4 and the carla 5 move toward both sides of the wrist 200, and the wrist.
- the belt 4, the carla 5, and the device body 3 move in close contact with both sides of the 200.
- the carla 5 may be configured to indirectly contact the skin of the wrist 200 via, for example, the seat members 86 and 106, as long as the skin of the wrist 200 can be pulled.
- the sensing cuff 73 is supplied with a predetermined amount of air so that the internal pressure becomes the pressure required for measuring blood pressure, is inflated, and is pressed onto the wrist 200 by the back plate 72 pressed by the pressing cuff 71. Pressed towards. Therefore, the sensing cuff 73 presses the artery 210 in the wrist 200 and occludes the artery 210 as shown in FIG.
- control unit 55 controls, for example, the third on-off valve 16C and repeatedly opens and closes the third on-off valve 16C, or adjusts the opening degree of the third on-off valve 16C to adjust the inside of the pressing cuff 71. Pressurize the pressure in the space. Based on the electric signal output from the second pressure sensor 17B in the process of pressurization, the control unit 55 obtains measurement results such as blood pressure values such as systolic blood pressure and diastolic blood pressure and heart rate (step ST66). The control unit 55 outputs an image signal corresponding to the obtained measurement result to the display unit 12, and displays the measurement result on the display unit 12 (step ST67). Further, the control unit 55 opens the first on-off valve 16A, the second on-off valve 16B, the third on-off valve 16C, and the fourth on-off valve 16D after the blood pressure measurement is completed.
- the display unit 12 When the display unit 12 receives the image signal, the display unit 12 displays the measurement result on the screen. The user confirms the measurement result by visually recognizing the display unit 12. After the measurement is completed, the user removes the rod 61f attached from the small hole 62a, removes the second belt 62 from the frame-shaped body 61e, and pulls out the wrist 200 from the carla 5, so that the blood pressure measuring device 1 is removed from the wrist 200. Remove.
- the joint allowance 94 of the sensing cuff 73 is pressed by the joint portion 94a to the welded portion 81a of the air bag 81 of the pressing cuff 71, in other words, to the outer edge portion of the air bag 81.
- the pressing cuff 71 and the sensing cuff 73 are fixed and integrated to form the cuff unit 250.
- the pressing cuff 71 and the sensing cuff 73 can be fixed to the carla 5 as an integral body. Will be.
- the pressing cuff 71 and the sensing cuff 73 can be fixed by one attachment work to the carla 5, the pressing cuff 71 and the sensing cuff 73 can be fixed to the carla 5 separately as compared with the configuration in which the pressing cuff 71 and the sensing cuff 73 are separately fixed to the carla 5.
- the misalignment of the pressing cuff 71 and the sensing cuff 73 can be suppressed.
- the cuff unit 250 it is not necessary to fix the pressing cuff 71, the back plate 72, and the sensing cuff 73 to the carla 5, respectively, so that the work efficiency of manufacturing the blood pressure measuring device 1 is improved. Can be improved.
- the joining allowance 94 is integrally formed with the sensing cuff 73, it is possible to suppress an increase in the number of parts of the cuff unit 250.
- the joining allowance 94 is joined to the air bag 81 adjacent to the air bag 91 of the sensing cuff 73 among the plurality of air bags 81 of the pressing cuff 71, so that the expansion of the pressing cuff 71 is hindered by the joining allowance 94. There is nothing to do.
- the joint allowance 94 is formed at the outer edge portion of the sensing cuff 73 along the longitudinal direction of the air bag 91, and the joint portion 94a of the joint allowance 94 is in the longitudinal direction of the air bag 81 on the back plate 72 side of the pressing cuff 71.
- the joined portion 94a is joined to a wide range of the welded portion 81a of the air bag 81 and a range facing the outside of the carla 5. As a result, it is possible to prevent water such as sweat from the user from entering between the pressing cuff 71 and the sensing cuff 73.
- the cuff unit 250 is manufactured by the jig 400 and has a shape that is curved according to the surface to which the pressing cuff 71 of the carla 5 is joined before being removed from the jig 400 and fixed to the carla 5. It is composed of. Therefore, when the cuff unit 250 is joined to the carla 5, it is possible to prevent the pressing cuff 71 and the sensing cuff 73 from having wrinkles that inhibit expansion.
- the cuff unit 250 is configured to include the back plate 72, the integrated body of the pressing cuff 71, the back plate 72, and the sensing cuff 73 can be fixed to the carla 5 by one attachment work, so that the blood pressure measuring device 1 can be used. The number of manufacturing processes can be reduced.
- the pressing cuff 71 and the sensing cuff 73 are integrally fixed by using the jig 400 having the mounting surface 401 formed on the curved surface corresponding to the surface on which the pressing cuff 71 is fixed.
- the cuff 71 and the sensing cuff 73 can be integrally fixed in a curved posture.
- the air bag 81 of the pressing cuff 71 and the air bag 91 of the sensing cuff 73 are wrinkled and the air bag 81 is formed. , 91 can be prevented from occurring in a state where the expansion is inhibited.
- the cuff unit is aligned with the flat mounting surface and the sensing cuff.
- the upper surface of 73 is configured to be flat.
- the cuff unit 250 is fixed to the carla 5 by using a jig 400 having a mounting surface 401 to integrate the pressing cuff 71 and the sensing cuff 73 by fixing by joining with a joining allowance 94. Occasionally, it is possible to prevent the air bags 81 and 91 from having wrinkles that inhibit expansion.
- the jig 400 has a plurality of positioning pins 402
- the first structure 251 has a plurality of pin holes 71a
- the second structure 252 has a plurality of pin holes 73a. Then, the first structure 251 and the second structure 252 are fixed and integrated in a state where they are set on the pin 402 and positioned. Therefore, it is possible to suppress the occurrence of misalignment of the sensing cuff 73 with respect to the pressing cuff 71.
- the pin hole 71a is also used for positioning the mold 302 with the pin 301 in the mold 302 in the process of manufacturing the first structure 251. Therefore, the position of the pressing cuff 71 with respect to the pin hole 71a is fixed.
- the pin hole 73a is used for positioning the mold 320 to the mold 320 by the pin 321 in the step of manufacturing the second structure 252. Therefore, the position of the sensing cuff 73 with respect to the pin hole 73a is fixed. As described above, by using the pin holes 71a and 73a in the manufacturing process of the structures 251, 252 and the manufacturing process of the cuff unit 250, the displacement of the sensing cuff 73 with respect to the pressing cuff 71 is further reduced. Can be suppressed.
- a plurality of positioning pins 402 are provided, a plurality of pin holes 71a and 73a are provided, and a plurality of positioning pins 402 are set in the plurality of pin holes 71a and 73a, whereby the mounting surface 401 is provided. It is possible to prevent the structures 251, 252 from moving such as rotating around the positioning pin 402.
- the work efficiency of manufacturing the cuff unit 250 can be improved.
- the joint allowance 94 of the sensing cuff 73 is provided by the joint portion 94a at two edges along the longitudinal direction of the air bag 81 on the back plate 72 side of the pressing cuff 71.
- the configuration joined to the welded portion 81a has been described as an example, but the present invention is not limited to this.
- the sensing cuff 73 may be fixed to the pressing cuff 71 by, for example, a joint portion 94a formed in an annular shape surrounding the air bag 81. In this configuration, the bonding allowance 94 is continuously formed in the welding portion 91a of the air bag 91 and the welding portion 92a of the flow path body 92.
- the outer edge portion along the longitudinal direction of the joining allowance 94 is joined to the welded portion 81a along the longitudinal direction of the air bag 81.
- the outer edge portion of the joining allowance 94 along the lateral direction is joined to the welded portion 81a along the lateral direction of the air bag 81.
- a part of the flow path body 92 is fixed to a part of the welded portion 81a of the air bag 81 on the back plate 72 side of the pressing cuff 71.
- the flow path body 92 and the welded portion 81a may be fixed by a fixing means other than welding. This fixing means is, for example, double-sided tape or an adhesive.
- the first structure 251 and the second structure 252 are manufactured separately and the joining allowance 94 of the second structure 252 is joined to the first structure 251 will be described as an example. However, it is not limited to this.
- the first sheet 86A and the second sheet 86B constituting the air bag 81 on the sensing cuff 73 side of the pressing cuff 71 are formed.
- the bonding allowance 94 of the second structure 252 may also be welded and bonded at the same time.
- the welded portion 81a and the joint portion 94a may be formed by one welding.
- the welded second sheet 86B and the third sheet 86C are arranged on the mold 302, the first sheet 86A is arranged on the second sheet 86B, and further, the first sheet 86A is arranged.
- the second structure 252 is arranged on the sheet 86A.
- the pin holes 71a and 73a are arranged and positioned at the pins 301 of the mold 302.
- the welding portion 81a and the joining portion 94a are formed.
- the second structure 252 shows only the vicinity of the joint portion 94a, and other configurations are omitted.
- the joining allowance 94 is composed of two sheet members 96a and 96b constituting the sensing cuff 73
- the joining allowance 94 may be formed on the sheet member 96a or the sheet member 96b, for example, as shown in FIGS. 52 and 53.
- the joining allowance 94 is formed on the fifth sheet member 96a arranged on the wrist 200 side, so that a step due to the thickness of the sheet member 96a is formed on the surface of the sensing cuff 73 on the wrist 200 side.
- the formation is suppressed. Therefore, it is possible to suppress the formation of a gap between the wrist 200 and the sensing cuff 73 due to this step, so that it is possible to suppress a decrease in the measurement accuracy of the blood pressure measuring device 1.
- the joint allowance 94 and the joint allowance 94 may be formed at the same time by simultaneously welding the first sheet 86A and the second sheet 86B constituting the air bag 81. In this case, the three sheets are welded at the same time.
- the first structure 251 and the second structure 252 are joined by the joining portion 94a of the joining allowance 94 to be integrated, and then the pressing cuff 71 is cut.
- An example of manufacturing by a manufacturing method of forming the shape of the sensing cuff 73 and forming the shape of the sensing cuff 73 has been described, but the present invention is not limited thereto.
- the first structure 251 is cut to form a shape close to the pressing cuff 71
- the second structure 252 is formed.
- the body 252 may be cut to form a shape close to that of the sensing cuff 73, and these may be integrally fixed by joining with a joining portion 94a using a jig 400.
- the shape close to the pressing cuff 71 referred to here is a shape that leaves a cutting allowance to the extent that a pin hole 71a is formed in the outer shape of the pressing cuff 71.
- the shape close to that of the sensing cuff 73 is a shape that leaves a cutting allowance to the extent that a pin hole 73a is formed in the outer shape of the sensing cuff 73. Then, after integrating the pressing cuff 71 and the sensing cuff 73, the cutting allowance forming the pin hole 71a and the cutting allowance forming the pin hole 73a are cut.
- the welding step (step ST14) of the sheet member of the first structure 251 is the second sheet 86B which is bridge-welded and integrated as shown in FIGS. 29 to 31.
- the first sheet 86A is welded and integrated to the second sheet 86B of the third sheet 86C
- the fourth sheet 86D is welded to the first sheet 86A, the second sheet 86B, and the third sheet 86C which are welded and integrated.
- the process is described as an example, but the present invention is not limited to this.
- step ST14 of the sheet member of the first structure 251
- the second sheet 86B of the second sheet 86B and the third sheet 86C integrated by bridge welding, and the welding of the first sheet 86A are performed.
- Welding of the third sheet 86C of the second sheet 86B and the third sheet 86C and the fourth sheet 86D which are bridge-welded and integrated may be performed in one step. As an example of this, there is the following method.
- an intermediate electrode is placed between the bridge-welded second sheet 86B and the third sheet 86C.
- the first sheet 86A, the second sheet 86B and the third sheet 86C in which the intermediate electrodes are arranged, and the fourth sheet 86D to which the connecting portion 84 is welded are sequentially set on the positioning pin of the jig, and the sheets 86A and 86B are sequentially set.
- 86C, 86D are placed on top of each other.
- the sheets 86A, 86B, 86C, 86D are welded to the outer peripheral shape of the pressing cuff 71 by a high frequency welding machine to form the welded portions 81a, 83a, and the sheets 86A, 86B, 86C, 86D are integrally welded. As a result, the air bag 81 and the flow path body 83 are formed.
- the configuration in which the bonding allowance 94 is bonded to the outer edge portion of the air bag 81 of the pressing cuff 71 is described as an example. Not limited to this.
- the joining allowance 94 may be fixed to the outer surface of the air bag 81 in a region inside the outer edge and around the outer edge.
- the region on the outer surface of the air bag 81 that is inside the outer edge and is around the outer edge is an example of the outer edge portion of the air bag 81.
- the present invention is not limited to the above-described embodiment.
- a configuration in which thermal welding is used as a joining means for joining the joining allowance 94 of the sensing cuff 73 to the pressing cuff 71 has been described as an example, but the present invention is not limited to this. In other examples, welding other than heat may be used. Further, in another example, the bonding means may be an adhesive or double-sided tape.
- the back plate 72 is arranged on the first structure 251 and fixed by the joint layer 75, and then the second structure 252 is arranged on the first structure 251 and the back plate 72.
- a manufacturing method in which the second structure and the back plate 72 are fixed by the bonding layer 75 and then the first structure 251 and the second structure 252 are integrally fixed by welding has been described as an example. Not limited.
- a back plate 72 may be arranged between 252 to fix the back plate 72 to the first structure 251 and the second structure 252.
- first structure 251 and the back plate 72 and the second structure 252 are sequentially arranged on the mounting surface 401 of the jig 400
- the present invention is limited to this. Not done.
- the first structure 251 and the back plate 72 are integrally fixed, these integral parts are set on the positioning pin 402 of the jig 400, and then the second structure 252 is set on the positioning pin 402.
- the back plate 72 and the second structure 252 may be fixed, and then the first structure 251 and the second structure 252 may be fixed and integrated by welding.
- the first structure 251 and the second structure 252 are respectively formed into a flat plate shape and then mounted on the mounting surface 401 of the jig 400, whereby the first structure 251 and the second structure 252 are mounted on the mounting surface 401.
- An example of being curved along is described as an example, but is not limited thereto.
- the first structure 251 and the second structure 252 are each formed by a mold having a mounting surface formed on a curved surface corresponding to a surface on which the pressing cuff 71 of the carla 5 is arranged.
- the welded portions 81a, 83a, 91a, 92a may be formed in a state of being curved along a curved surface corresponding to the surface on which the pressing cuff 71 is arranged.
- the back plate 72 is fixed to the pressing cuff 71 and the sensing cuff 73 by the bonding layer 75 made of double-sided tape, but the present invention is not limited to this. ..
- the back plate 72 may be fixed by a fixing means other than double-sided tape such as an adhesive.
- the mounting surface 401 of the jig 400 has a configuration in which at least the entire area of the air bag 81 and the air bag 91 can be arranged, and the entire area of the air bag 81, the entire area of the air bag 91, and the flow path body 83.
- a configuration having a size capable of arranging a part and a part of the flow path body 92 has been described as an example, but the present invention is not limited to this.
- the mounting surface 401 may have a size capable of arranging the entire area of the air bag 81, the entire area of the flow path body 83, the entire area of the air bag 91, and the entire area of the flow path body 92.
- the pressing cuff 71 has been described as an example of a configuration including a plurality of air bags 81 and a configuration including two air bags 81, but the present invention is not limited to this.
- the pressing cuff 71 may be configured to include, for example, three or more air bags 81.
- the present invention is not limited to the above embodiment, and can be variously modified at the implementation stage without departing from the gist thereof.
- each embodiment may be carried out in combination as appropriate as possible, in which case the combined effect can be obtained.
- the above-described embodiment includes inventions at various stages, and various inventions can be extracted by an appropriate combination in a plurality of disclosed constituent requirements.
- Control unit 56 Main CPU 57 ... Sub CPU 61 ... 1st belt 61a ... Belt part 61b ... Buckle 61c ... 1st hole part 61d ... 2nd hole part 61e ... Frame-shaped body 61f ... Tsukuba rod 62 ... 2nd belt 62a ... Small hole 62b ... 3rd hole part 71 ... Pressing cuff 71a ... Pin hole 72 ... Back plate 72a ... Groove 73 ... Sensing cuff 73a ... Pin hole 74 ... Tension cuff 75 ... Bonding layer 81 ... Air bag (first bag-shaped structure) 81a ... Welding part 81b ...
- Bridge welding part 82 ... Jointed part 83 ... Flow path body 83a ... Welding part 84 ... Connecting part 86 ... Sheet member 86a ... First sheet member 86b ... Second sheet member 86b1 ... Opening 86c ... Third Sheet member 86c1 ... Opening 86d ... Fourth sheet member 86d1 ... Hole 91 ... Air bag (second bag-shaped structure) 91a ... Welding part 92 ... Flow path body 92a ... Welding part 93 ... Connecting part 94 ... Joining allowance 94a ... Joining part 96 ... Sheet member 96a ... 5th sheet member 96b ... 6th sheet member 96b1 ...
Landscapes
- Health & Medical Sciences (AREA)
- Life Sciences & Earth Sciences (AREA)
- Surgery (AREA)
- Animal Behavior & Ethology (AREA)
- Pathology (AREA)
- Engineering & Computer Science (AREA)
- Biomedical Technology (AREA)
- Heart & Thoracic Surgery (AREA)
- Medical Informatics (AREA)
- Molecular Biology (AREA)
- Physics & Mathematics (AREA)
- Biophysics (AREA)
- General Health & Medical Sciences (AREA)
- Public Health (AREA)
- Veterinary Medicine (AREA)
- Cardiology (AREA)
- Vascular Medicine (AREA)
- Physiology (AREA)
- Ophthalmology & Optometry (AREA)
- Dentistry (AREA)
- Measuring Pulse, Heart Rate, Blood Pressure Or Blood Flow (AREA)
Abstract
カーラに対する押圧カフ及びセンシングカフのそれぞれの位置ずれを抑制できるカフユニット、カフユニットの製造方法、及び血圧測定装置を提供する。 カフユニット(250)は、積層され、それぞれが流体により膨張する複数の空気袋(81)を含み、カーラ(5)に接合される押圧カフ(71)と、流体により膨張する1つの空気袋(91)、及び空気袋(91)に形成され、前記空気袋(91)に隣接する空気袋(81)に接合される接合代(94)を含むセンシングカフ(73)と、を備える。
Description
本発明は、血圧測定装置に用いられるカフユニット、このカフユニットの製造方法、及び血圧測定装置に関する。
近年、血圧の測定に用いる血圧測定装置は、医療設備においてのみならず、家庭内においても、健康状態を確認する手段として利用されている。血圧測定装置は、例えば、生体の上腕又は手首等に巻き付けたカフを膨張及び収縮させ、圧力センサによりカフの圧力を検出することで、動脈壁の振動を検出して血圧を測定する。このような血圧測定装置に用いられるカフとして、例えば、日本国特開平11-309119号公報に開示されるように、複数の空気袋を膨張させて動脈を圧迫する技術が知られている(例えば、特許文献1参照)。
手首に装着される態様を有する血圧測定装置では、血管の圧閉方向にセンシングカフが膨張し、膨張時にセンシングカフが手首に密着することが求められる。そこで、膨張したセンシングカフを手首に密着させるために、血圧測定装置を手首に固定するベルトとセンシングカフとの間にカーラを用いる技術が知られている。
また、このような血圧測定装置は、センシングカフを手首に密着させるために、カーラの内周面に、センシングカフを手首に押圧する押圧カフを固定する構成が考えられる。
しかしながら、カーラに押圧カフ及びセンシングカフを積層して配置する構成を有する血圧測定装置では、カーラに対して、押圧カフ及びセンシングカフを順番に接合すると、カーラに対して押圧カフ及びセンシングカフのそれぞれに位置ずれが生じる。押圧カフ及びセンシングカフのそれぞれに位置ずれが生じることで、カーラに対するセンシングカフの位置ずれが大きくなる可能性がある。カーラに対してセンシングカフの位置ずれが大きくなると、血圧測定の精度が低下する虞がある。
そこで本発明は、カーラに対する押圧カフ及びセンシングカフのそれぞれの位置ずれを抑制できるカフユニット、カフユニットの製造方法、及び血圧測定装置を提供することを目的とする。
一態様によれば、積層され、それぞれが流体により膨張する複数の第1袋状構造体を含み、カーラに接合される押圧カフと、流体により膨張する1つの第2袋状構造体、及び前記第2袋状構造体に形成され、前記第2袋状構造体に隣接する前記第1袋状構造体に接合される接合代を含むセンシングカフと、を備えるカフユニットが提供される。
ここで、カフとは、血圧を測定するときに生体の手首等に巻き付けられ、流体が供給されることで膨張する一つ又は多層の袋状構造体を含む。袋状構造体とは、流体により膨張するものであり、流体が空気である場合には空気袋である。
この態様によれば、押圧カフ及びセンシングカフを接合代により接合することで一体化したカフユニットを構成することで、押圧カフ及びセンシングカフを、一体物として、カーラに固定することが可能となる。この為、カーラに対する一度の取り付け作業で、押圧カフ及びセンシングカフを固定できるので、押圧カフ及びセンシングカフを別々にカーラに対して固定する構成に比較して、カーラに対する押圧カフ及びセンシングカフの位置ずれを抑制できる。さらに、押圧カフの膨張が接合代により阻害されることを抑制できる。
上記一態様のカフユニットにおいて、前記第1袋状構造体は、一方向に長い形状に構成され、前記第2袋状構造体は、一方向に長い形状に構成され、前記接合代は、前記第2袋状構造体の長手方向に沿う外縁部に形成され、前記第1袋状構造体の長手方向に沿う外縁部に接合される、カフユニットが提供される。
この態様によれば、接合代が、第1袋状構造体の広い範囲に接合される。結果、押圧カフ及びセンシングカフの間に、ユーザの汗等の水が浸入することを抑制できる。
上記一態様のカフユニットにおいて、前記押圧カフ及び前記センシングカフは、前記カーラの内周面にならって湾曲する、カフユニットが提供される。
この態様によれば、カフユニットをカーラに接合したときに、押圧カフ及びセンシングカフに、膨張を阻害するしわが発生することを抑制できる。
上記一態様のカフユニットにおいて、前記押圧カフ及び前記センシングカフの間に配置され、前記押圧カフ及び前記センシングカフに接合される背板を備える、カフユニットが提供される。
この態様によれば、押圧カフ、背板、及びセンシングカフの一体物をカーラに一度の取り付け作業で固定できるので、血圧測定装置の製造工程数を低減できる。
一態様によれば、カーラの押圧カフが接合される面に対応する曲面に形成された載置面を有する冶具の前記載置面に、前記押圧カフを含む第1構造体を配置して前記載置面に対する前記第1構造体の位置決めをし、前記第1構造体上に、センシングカフを含む第2構造体を配置して前記載置面に対する前記第2構造体の位置決めをし、前記第1構造体及び前記第2構造体を接合して一体化する、カフユニットの製造方法が提供される。
ここで、カーラの押圧カフが固定される面に対応する曲面に形成された載置面とは、当該載置面に沿って形成されるカフユニットをカーラに固定したときに、カフユニットがカーラに固定する前に比較して湾曲することで押圧カフ及びセンシングカフの少なくとも一方に、膨張を阻害するしわが発生することを抑制できる曲面である。カーラの、押圧カフが配置される面に対応する曲面は、例えば、カーラの、押圧カフが配置される面と同じ曲率を有する曲面である。他の例では、カーラの、押圧カフが配置される面に対応する曲面は、カーラの、押圧カフが配置される面と略同じ曲率を有する曲面である。
この態様によれば、カーラの、押圧カフが固定される面に対応する曲面に構成された載置面を有する冶具を用いて、押圧カフ及びセンシングカフを一体に固定することで、押圧カフ及びセンシングカフを、湾曲した姿勢で、一体に固定できる。結果、押圧カフ及びセンシングカフが一体に固定されたカフユニットをカーラに固定したときに、押圧カフ及びセンシングカフにしわが生じて押圧カフ及びセンシングカフの膨張が阻害されるという状態が生じることを抑制できる。すなわち、押圧カフ及びセンシングカフを、平面状の載置面を有する冶具を用いて一体に固定してカフユニットを構成すると、カフユニットは、平面状の載置面に合わせて、センシングカフの上面が平面となる形状に構成される。このカフユニットをカーラに固定すると、カフユニットがカーラの形状に合わせて湾曲することで生じる内外周差によって、押圧カフ及びセンシングカフにしわが生じる可能性がある。
しかしながら、湾曲する載置面を有する冶具を用いて、押圧カフ及びセンシングカフを固定して一体化することで、カフユニットをカーラに固定したときに、押圧カフ及びセンシングカフに、膨張を阻害するしわが発生することを抑制できる。
上記一態様のカフユニットの製造方法において、前記第2構造体は、接合代を含み、前記第1構造体及び前記第2構造体は、前記接合代で接合される、カフユニットの製造方法が提供される。
この態様によれば、第1構造体及び前記第2構造体の接合に、別部品を必要としないので、第1構造体及び第2構造体の一体部の部品数が増えることを抑制できる。
上記一態様のカフユニットの製造方法において、前記第1構造体上に背板を配置して前記背板を前記第1構造体に接合した後、前記第1構造体及び前記背板上に前記第2構造体を配置して、前記第2構造体を前記第1構造体及び前記背板に接合する、カフユニットの製造方法が提供される。
この態様によれば、押圧カフ、背板、及びセンシングカフの一体物をカーラに一度の取り付け作業で固定できるので、血圧測定装置の製造工程数を低減できる。
上記一態様のカフユニットの製造方法において、前記冶具は、複数の位置決めピンを有し、前記第1構造体は、前記位置決めピンを配置する孔を複数有し、前記第2構造体は、前記位置決めピンを配置する孔を複数有し、前記複数の位置決めピンが、前記第1構造体の複数の前記孔、及び前記第2構造体の複数の前記孔にセットされた状態で、前記接合代が前記第1構造体に接合される、カフユニットの製造方法が提供される。
この態様によれば、載置面に対して、第1構造体及び第2構造体が位置決めピン回りに回転する等の移動することを抑制できる。
上記一態様のカフユニットの製造方法において、前記第1構造体及び前記第2構造体は、それぞれ、裁断代を含み、前記第1構造体、及び前記第2構造体を固定して一体化した後に、前記裁断代を裁断する、カフユニットの製造方法が提供される。
この態様によれば、第1構造体及び第2構造体を固定して一体化した後に裁断を行うことで、カフユニットの製造の作業効率を向上できる。
一態様によれば、カーラと、積層され、それぞれが流体により膨張する複数の第1袋状構造体を含み、カーラに接合される押圧カフ、並びに、流体により膨張する1つの第2袋状構造体、及び前記第2袋状構造体に形成され、前記第2袋状構造体に隣接する前記第1袋状構造体に接合される接合代を含むセンシングカフを備えるカフユニットと、前記カフユニットに前記流体を供給する装置本体と、を備える血圧測定装置が提供される。
この態様によれば、押圧カフ及びセンシングカフを接合代により接合することで一体化したカフユニットを構成することで、押圧カフ及びセンシングカフを、一体物として、カーラに固定することが可能となる。この為、カーラに対する一度の取り付け作業で、押圧カフ及びセンシングカフを固定できるので、押圧カフ及びセンシングカフを別々にカーラに対して固定する構成に比較して、カーラに対する押圧カフ及びセンシングカフの位置ずれを抑制できる。さらに、押圧カフの膨張が接合代により阻害されることを抑制できる。
本発明は、カーラに対する押圧カフ及びセンシングカフのそれぞれの位置ずれを抑制できるカフユニット、カフユニットの製造方法、及び血圧測定装置を提供できる。
以下、本発明の一実施形態に係る血圧測定装置1の一例について、図1乃至図21を用いて以下例示する。
図1は、本実施形態に係る血圧測定装置1の構成を示す斜視図である。図2は、血圧測定装置1の構成を分解して示す斜視図である。図3は、血圧測定装置1の構成を示す側面図である。図4は、血圧測定装置1を手首200に装着した状態を示す説明図である。図5は、血圧測定装置1の構成を示すブロック図である。図6は、血圧測定装置1の一部の構成を省略して示す斜視図である。図7は、血圧測定装置1のカーラ5及びカフ構造体6の構成を示す分解して示す斜視図である。図8は、血圧測定装置1のカーラ5及びカフユニット250の構成を示す断面図である。図9は、血圧測定装置1のカーラ5及びカフユニット250の構成を示す断面図である。図10は、血圧測定装置1の引張カフ74の構成を示す断面図である。図11は、血圧測定装置1の引張カフ74の構成を示す断面図である。図12は、血圧測定装置1のカーラ5の構成を示す斜視図である。図13は、血圧測定装置1のカフ構造体6の手首200側の構成示す平面図である。図14は、カフ構造体6のカーラ5の内周面側の構成を示す平面図である。
図15は、血圧測定装置1の押圧カフ71の構成を示す平面図である。図16は、押圧カフ71の構成を図15中XVI-XVI線断面で示す断面図である。図17は、血圧測定装置1のセンシングカフ73の構成を示す平面図である。図18は、血圧測定装置1のセンシングカフ73の構成を図17中XVIII-XVIII線断面で示す断面図である。図19は、血圧測定装置1のカフユニット250の構成を示す平面図である。図20は、血圧測定装置1の引張カフ74の構成を示す平面図である。図21は、引張カフ74の構成を示す断面図である。
血圧測定装置1は、生体に装着する電子血圧測定装置である。本実施形態においては、生体の手首200に装着するウェアラブルデバイスの態様をもつ電子血圧測定装置を用いて説明する。
図1乃至図6に示すように、血圧測定装置1は、装置本体3と、手首に装置本体3を固定するベルト4と、ベルト4及び手首の間に配置されるカーラ5と、押圧カフ71、センシングカフ73及び引張カフ74を有するカフ構造体6と、装置本体3及びカフ構造体6を流体的に接続する流体回路7と、カーラ5に設けられた給電部8と、を備えている。
図1乃至図6に示すように、装置本体3は、例えば、ケース11と、表示部12と、操作部13と、ポンプ14と、流路部15と、開閉弁16と、圧力センサ17と、電力供給部18と、振動モータ19と、制御基板20と、を備えている。装置本体3は、ポンプ14、開閉弁16、圧力センサ17及び制御基板20等によって、カフ構造体6に流体を供給する。
図1乃至図3に示すように、ケース11は、筒状の外郭ケース31と、外郭ケース31の手首200側とは反対側(外方側)の開口を覆う風防32と、外郭ケース31の内部の手首200側に設けられた基部33と、外郭ケース31の手首200側を覆う裏カバー35と、裏カバー35の下面に設けられるシール部材36と、を備えている。
外郭ケース31は、例えば円筒状に形成される。外郭ケース31は、外周面の周方向で対称位置にそれぞれ設けられた一対のラグ31aと、2つの一対のラグ31a間にそれぞれ設けられるバネ棒31bと、を備えている。風防32は、例えば、円形状のガラス板である。
基部33は、表示部12、操作部13、ポンプ14、開閉弁16、圧力センサ17、電力供給部18、振動モータ19及び制御基板20を保持する。また、基部33は、例えば、ポンプ14及びカフ構造体6を流体的に連続する流路部15の一部を構成する。
裏カバー35は、中央側が開口する環状に構成される。裏カバー35は、外郭ケース31の手首200側の端部の外周縁側を覆う。このような裏カバー35は、カーラ5と一体に組み合わされることで、中央の開口がカーラ5により覆われ、そしてカーラ5とともに外郭ケース31の手首200側の端部を覆う裏蓋を構成する。具体的には、裏カバー35は、4つの第1締結部材35aによってカーラ5に固定されるとともに、4つの第2締結部材35bによって外郭ケース31の手首200側の端部に固定される。裏カバー35は、底部に設けられ、カーラ5に固定される第1締結部材35aを挿通する4つの孔部35cと、外周部の4箇所が径方向に突出し、この突出した部位に設けられた外郭ケース31に固定される第2締結部材35bを挿通する4つの孔部35dと、を有する。
第1締結部材35a及び第2締結部材35bは、螺子、ボルト、ビス、リベット等の二つの部品を機械的に締結する部材である。本実施形態において、第1締結部材35a及び第2締結部材35bは、ネジである。
シール部材36は、裏カバー35のカーラ5と接触する領域の形状に形成された、例えば両面テープである。シール部材36は、カーラ5及び裏カバー35の間に存することで、カーラ5及び裏カバー35間をシールする。
表示部12は、外郭ケース31の基部33上であって、且つ、風防32の直下に配置される。図5に示すように、表示部12は、電気的に制御基板20に接続される。表示部12は、例えば、液晶ディスプレイ又は有機エレクトロルミネッセンスディスプレイである。表示部12は、日時や最高血圧及び最低血圧などの血圧値や心拍数等の測定結果を含む各種情報を表示する。
操作部13は、使用者からの指令を入力可能に構成される。例えば、操作部13は、図1及び図5に示すように、ケース11に設けられた複数の釦41と、釦41の操作を検出するセンサ42と、表示部12又は風防32に設けられたタッチパネル43と、を備える。操作部13は、使用者が操作することで、指令を電気信号に変換する。センサ42及びタッチパネル43は、電気的に制御基板20に接続され、電気信号を制御基板20へ出力する。
複数の釦41は、例えば3つ設けられる。釦41は、基部33に支持されるとともに、外郭ケース31の外周面から突出する。複数の釦41及び複数のセンサ42は、基部33に支持される。タッチパネル43は、例えば、風防32に一体に設けられる。
ポンプ14は、例えば圧電ポンプである。ポンプ14は、空気を圧縮し、流路部15を介して圧縮空気をカフ構造体6に供給する。ポンプ14は、電気的に制御基板20に接続される。
流路部15は、図5に示すように、ポンプ14から押圧カフ71及び引張カフ74へつながる流路、及び、ポンプ14からセンシングカフ73へつながる流路を構成する。また、流路部15は、押圧カフ71及び引張カフ74から大気へつながる流路、及び、センシングカフ73から大気へつながる流路を構成する。流路部15は、基部33等に設けられた中空部、溝、流路タンク及びチューブ等により構成された空気の流路である。
開閉弁16は、流路部15の一部を開閉する。開閉弁16は、複数、具体例として、図5に示すように、4つ設けられ、各開閉弁16の開閉の組み合わせによりポンプ14から押圧カフ71及び引張カフ74へつながる流路、ポンプ14からセンシングカフ73へつながる流路、押圧カフ71及び引張カフ74から大気へつながる流路、及び、センシングカフ73から大気へつながる流路を選択的に開閉する。具体例として、4つの開閉弁16は、第1開閉弁16A、第2開閉弁16B、第3開閉弁16C及び第4開閉弁16Dにより構成される。第1開閉弁16Aは、ポンプ14とセンシングカフ73とを接続する流路を開閉する。第2開閉弁16Bは、ポンプ14と引張カフ74とを接続する流路を開閉する。第2開閉弁16B及び第3開閉弁16Cは、ポンプ14と押圧カフ71とを接続する流路を開閉する。第2開閉弁16B、第3開閉弁16C及び第4開閉弁16Dは、ポンプ14及び大気を接続する流路を開閉する。
圧力センサ17は、少なくともセンシングカフ73の圧力を検出する。圧力センサ17は、例えば、第1圧力センサ17A及び第2圧力センサ17Bを備える。圧力センサ17は、検出した圧力を電気信号に変換し、制御基板20へ出力する。例えば、第1圧力センサ17A及び第2圧力センサ17Bは、流路部15の第1圧力センサ17A及びセンシングカフ73を接続する流路に設けられる。この流路は押圧カフ71、センシングカフ73及び引張カフ74とポンプ14とが、各開閉弁の開閉によって連続することから、これら流路内の圧力がポンプ14のつながる押圧カフ71、センシングカフ73及び引張カフ74の内部空間の圧力となる。
具体例として圧力センサ17は、第1開閉弁16Aが開であり、そして、第2開閉弁16Bを閉であるときにセンシングカフ73の圧力、換言すると、ポンプ14及びセンシングカフ73を接続する流路部15の圧力を検出する。また、圧力センサ17は、第1開閉弁16A及び第2開閉弁16Bが開であり、そして、第3開閉弁16Cが閉であるときに、センシングカフ73及び引張カフ74の圧力、換言すると、ポンプ14、センシングカフ73及び引張カフ74を接続する流路部15の圧力を検出する。さらに、圧力センサ17は、第1開閉弁16A、第2開閉弁16B及び第3開閉弁16Cが開であり、そして、第4開閉弁16Dが開又は閉であるときに、押圧カフ71、センシングカフ73及び引張カフ74の圧力、換言すると、ポンプ14、押圧カフ71、センシングカフ73及び引張カフ74を接続する流路部15の圧力を検出する。
電力供給部18は、例えば、リチウムイオンバッテリ等の二次電池である。電力供給部18は、図5に示すように、制御基板20に電気的に接続される。電力供給部18は、制御基板20に電力を供給する。
図5に示すように、制御基板20は、例えば、基板51と、加速度センサ52と、通信部53と、記憶部54と、制御部55と、を備えている。制御基板20は、加速度センサ52、通信部53、記憶部54及び制御部55が基板51に実装されることで構成される。
基板51は、ケース11の基部33にビス等によって固定される。
加速度センサ52は、例えば、3軸加速度センサである。加速度センサ52は、装置本体3の互いに直交する3方向の加速度を表す加速度信号を制御部55に出力する。例えば、加速度センサ52は、検出された加速度から血圧測定装置1を装着した生体の活動量を測定するために用いられる。
通信部53は、外部の装置と無線又は有線によって情報を送受信可能に構成される。通信部53は、例えば、制御部55によって制御された情報や測定された血圧値及び脈拍等の情報を、ネットワークを介して外部の装置へ送信し、また、外部の装置からネットワークを介してソフトウェア更新用のプログラム等を受信して制御部に送る。
本実施形態において、ネットワークは、例えばインターネットであるが、これに限定されず、病院内に設けられたLAN(Local Area Network)等のネットワークであってもよく、また、USB等の所定の規格の端子を有するケーブルなどを用いた外部の装置との直接的な通信であってもよい。このため、通信部53は、無線アンテナ及びマイクロUSBコネクタ等の複数を含む構成であってもよい。
記憶部54は、血圧測定装置1全体及び流体回路7を制御するためのプログラムデータ、血圧測定装置1の各種機能を設定するための設定データ、圧力センサ17で測定された圧力から血圧値や脈拍を算出するための算出データ等を予め記憶する。また、記憶部54は、測定された血圧値や脈拍等の情報を記憶する。
制御部55は、単数又は複数のCPUにより構成され、血圧測定装置1全体の動作、及び、流体回路7の動作を制御する。制御部55は、表示部12、操作部13、ポンプ14、各開閉弁16及び各圧力センサ17に電気的に接続されるとともに、電力を供給する。また、制御部55は、操作部13及び圧力センサ17が出力する電気信号に基づいて、表示部12、ポンプ14及び開閉弁16の動作を制御する。
例えば、制御部55は、図5に示すように、血圧測定装置1全体の動作を制御するメインCPU(Central Processing Unit)56及び流体回路7の動作を制御するサブCPU57を有する。例えば、メインCPU56は、圧力センサ17が出力する電気信号から、最高血圧及び最低血圧などの血圧値や心拍数などの測定結果を求め、この測定結果に対応した画像信号を表示部12へ出力する。
例えば、サブCPU57は、操作部13から血圧を測定する指令が入力されると、ポンプ14及び開閉弁16を駆動して押圧カフ71及びセンシングカフ73に圧縮空気を送る。また、サブCPU57は、圧力センサ17が出力する電気信号に基づいて、ポンプ14の駆動及び停止、並びに、開閉弁16の開閉を制御する。サブCPU57は、ポンプ14及び開閉弁16を制御することで、圧縮空気を押圧カフ71及びセンシングカフ73に選択的に送るとともに、押圧カフ71及びセンシングカフ73を選択的に減圧する。
図1乃至図4に示すように、ベルト4は、一方の一対のラグ31a及びバネ棒31bに設けられた第1ベルト61と、他方の一対のラグ31a及びバネ棒31bに設けられた第2ベルト62と、を備える。ベルト4は、カーラ5を介して手首200に巻き付けられる。
第1ベルト61は、所謂親と呼ばれ、第2ベルト62と連結可能な帯状に構成される。第1ベルト61は、図1乃至図3に示すように、ベルト部61a及び尾錠61bを有する。ベルト部61aは、帯状に構成される。ベルト部61aは、弾性変形可能な樹脂材料で形成される。また、ベルト部61aは、可撓性を有するとともに、ベルト部61aの長手方向の伸縮が抑制されるシート状のインサート部材を内部に有する。ベルト部61aは、一方の端部に形成され、ベルト部61aの長手方向に直交する第1孔部61c及び他方の端部に形成され、第1ベルト61の長手方向に直交する第2孔部61dを有する。
図4及び図6に示すように、第1孔部61cは、ベルト部61aの端部に設けられる。第1孔部61cは、バネ棒31bを挿入可能、且つ、バネ棒31bに関して第1ベルト61が回転可能な内径を有する。即ち、第1ベルト61は、一対のラグ31aの間であって、且つ、バネ棒31bに第1孔部61cが配置されることで、外郭ケース31に回転可能に保持される。
図1及び図3に示すように、第2孔部61dは、ベルト部61aの先端に設けられる。第2孔部61dは、尾錠61bが取り付けられる。
図1及び図3に示すように、尾錠61bは、矩形枠状の枠状体61eと、枠状体61eに回転可能に取り付けられたつく棒61fと、を有する。枠状体61eは、つく棒61fが取り付けられた一辺が第2孔部61dに挿入され、ベルト部61aに関して回転可能に取り付けられる。
第2ベルト62は、所謂剣先と呼ばれ、枠状体61eに挿入可能な幅を有する帯状に構成される。第2ベルト62は、弾性変形可能な樹脂材料で形成される。また、第2ベルト62は、可撓性を有するとともに、第2ベルト62の長手方向の伸縮が抑制されるシート状のインサート部材を内部に有する。
また、第2ベルト62は、図1及び図2に示すように、つく棒61fが挿入される小孔62aを複数有する。また、第2ベルト62は、一方の端部に設けられ、第2ベルト62の長手方向に直交する第3孔部62bを有する。第3孔部62bは、バネ棒31bを挿入可能、且つ、バネ棒31bに関して第2ベルト62が回転可能な内径を有する。即ち、第2ベルト62は、一対のラグ31aの間であって、且つ、バネ棒31bに第3孔部62bが配置されることで、外郭ケース31に回転可能に保持される。
このようなベルト4は、第2ベルト62が枠状体61eに挿入され、小孔62aにつく棒61fが挿入されることで、第1ベルト61及び第2ベルト62が一体に接続され、外郭ケース31とともに、手首200の周方向に倣った環状となる。ベルト4は、手首200の周方向に倣った環状となることで、カーラ5を押圧し、カーラ5を血圧測定装置1の装着者の手首の周方向に倣うように、弾性変形させる。
カーラ5は、図1乃至図4に示すように、手首200の周方向に倣って湾曲する帯状に構成される。カーラ5は、一端と他端が離間した形状に形成される。カーラ5は、例えば、一端側の外面が装置本体3の裏カバー35に固定される。カーラ5は、一端及び他端が裏カバー35よりも手首200の一方の側方側に突出した位置に配置される。これにより、カーラ5は、血圧測定装置1を手首200に装着したときに、一端及び他端が手首200の側方に配置される。また、カーラ5は、所定の距離だけ離間して一端及び他端が隣接する。カーラ5は、例えば、樹脂材料で形成される。具体例として、カーラ5は、ポリプロピレンによって厚さが1mm程度に形成される。
具体例として、図1乃至図4に示すように、カーラ5は、手首の周方向に倣って湾曲する帯状に構成される。また、カーラ5は、一端側の手首200の手の甲側に対向する位置に設けられ、裏カバー35とともに裏蓋を構成する円板状のカバー部5a、カバー部5aの周囲に設けられ、及び、外郭ケース31及び裏カバー35を固定する第2締結部材35bを移動可能な逃げ部5bを有する。カーラ5は、例えば、カバー部5a及びその隣接する部位が平板状に形成されるとともに、カバー部5aよりも一端側及び他端側が所定の曲率で湾曲して形成される。そして、カーラ5は、カバー部5aから一端までの長さが、カバー部5aから他端までの長さよりも短く形成される。具体例として、カーラ5は、カバー部5aから一端までの短手側が、手首の手の甲側に配置され、そして、カバー部5aから他端までの長手側が、手首の手の甲側から一方の側方を通って手首200の手の平側まで延びる。
また、図12に示すように、カーラ5は、一端及び他端が近接したときに、一端側の内周面側に他端が位置する形状に形成される。具体例として、カーラ5の手首200の幅方向の幅は、カーラ5の手首200の手の平側よりもカーラ5の手首200の手の甲側が大きく設定される。そして、カーラ5は、手首200の手の甲側の一端の曲率半径が手首200の手の平側の他端の曲率半径よりも大きく設定される。このような構成により、カーラ5は、カーラ5の両端側が当接すると、一端よりも他端がカーラ5の内方に配置される。また、カーラ5は、カバー部5aの一部、及び、カバー部5aから一端側の外面、さらに言えば、カバー部5aから延びる短手側の外面に、カバー部5aに隣接して設けられた窪み5cが設けられる。
カバー部5aは、インサートされた補強用のインサート部材5dを含む。カバー部5aは、固定された裏カバー35を介して外郭ケース31の手首200側に固定される。カバー部5aは、裏カバー35の4つの孔部35cと対向する位置に設けられ、裏カバー35を固定する第1締結部材35aが螺合される螺子孔5eを有する。さらに、カバー部5aは、カフ構造体6を装置本体3に接続するための3つ孔部5fを有する。
逃げ部5bは、裏カバー35側から外郭ケース31に裏カバー35を第2締結部材35bにより固定するときに、第2締結部材35bがカーラ5に干渉せずに第2締結部材35bを裏カバー35に配置するため及び第2締結部材35bを回転させる工具を配置するための逃げである。
3つの孔部5fは、押圧カフ71の後述する接続部84を挿入可能な内径に形成された第1孔部5f1、センシングカフ73の後述する接続部93を挿入可能な内径に形成された第2孔部5f2、及び、引張カフ74の後述する接続部103を挿入可能な内径に形成された第3孔部5f3である。本実施形態において、第2孔部5f2は、第1孔部5f1及び第3孔部5f3よりも、カバー部5a内のカーラ5の手の平側の他端側に配置される。
このようなカーラ5は、一端及び他端がベルト4の第2ベルト62と対向する向きで外郭ケース31に固定される。また、カーラ5は、少なくとも、手首200の手の平側と対向する位置が、手首200の手の平側に沿って周方向に沿って湾曲することで、手首200の手の平側と対向するカフ構造体6を、手首200の手の平側の形状に倣って湾曲させた状態で保持する。
また、カーラ5は、可撓性及び形状保持性を有する硬さを有する。ここで、可撓性とは、カーラ5にベルト4の外力が印加されたときに径方向に形状が変形することをいう。例えば、可撓性とは、ベルト4によってカーラ5が押圧されたときに、手首に近接するか、手首の形状に沿うか、又は、手首の形状に倣うように側面視の形状が変形することをいう。また、形状保持性とは、外力が印加されないときに、カーラ5が予め賦形された形状を維持できることをいう。例えば、形状保持性とは、本実施形態においてはカーラ5の形状が手首の周方向に沿って湾曲する形状を維持できることである。
カーラ5は、内周面にカフ構造体6が配置され、そして、カーラ5の内周面形状に沿ってカフ構造体6を保持する。具体例として、カーラ5は、押圧カフ71及び引張カフ74が内周面に配置され、カーラ5並びに押圧カフ71及び引張カフ74との間に設けられる接合層75により、カフ構造体6が固定されることで、カフ構造体6を保持する。本実施形態においては、接合層75は、接着剤や両面テープである。
図1乃至図6、図13及び図14に示すように、カフ構造体6は、押圧カフ71と、背板72と、センシングカフ73と、引張カフ74と、を備えている。また、カフ構造体6は、各構成同士、及び、カーラ5とカフ71、74を接合する接合層75を備えている。カフ構造体6は、カーラ5に固定される。カフ構造体6は、押圧カフ71、背板72及びセンシングカフ73が積層してカーラ5に配置され、引張カフ74が押圧カフ71、背板72及びセンシングカフ73と離間してカーラ5に配置される。
具体例として、カフ構造体6は、図4に示すように、カーラ5の手首200の手の平側の内周面に、カーラ5の内周面から手首200側に向かって、押圧カフ71、背板72及びセンシングカフ73の順に積層して固定される。また、カフ構造体6は、カーラ5の手首200の手の甲側の内周面に引張カフ74が配置される。カフ構造体6の各部材は、積層方向に隣接する部材に接合層75によって固定される。
押圧カフ71は、流路部15を介してポンプ14に流体的に接続される。押圧カフ71は、膨張することで背板72及びセンシングカフ73を手首200側に押圧する。押圧カフ71は、図8、図9、図13乃至図17に示すように、複数の、例えば二層の空気袋(第1袋状構造体)81と、カーラ5と対向する空気袋81に設けられた被接合部82と、空気袋81と連通する流路体83と、流路体83の先端に設けられた接続部84と、を含む。このような押圧カフ71は、複数のシート部材86を一体に溶着することで構成される。
ここで、空気袋81とは、袋状構造体であり、本実施形態においては血圧測定装置1がポンプ14により空気を用いる構成であることから、空気袋を用いて説明するが、空気以外の流体を用いる場合には、袋状構造体は当該流体により膨張する流体袋であればよい。複数の空気袋81は、積層され、積層方向に流体的に連通する。
空気袋81は、一方向に長い矩形状の袋形状に形成される。また、空気袋81は、短手方向の幅が、カーラ5の短手方向の幅と同じ幅に設定される。空気袋81は、例えば、二枚のシート部材86を組み合わせ、図8、図9、図13乃至図17に溶着部81aを示すように、一方向に長い矩形枠状に熱により溶着することで構成される。また、二層の空気袋81は、二つの空気袋81を熱により溶着して一体に組み合わせるか、又は、隣り合う空気袋81の対向するシート部材86同士を溶着した後に空気袋81を溶着して形成することで構成される。具体例として、二層の空気袋81は、互いに対向するシート部材86に設けられた開口によって流体的に連続する。また、二層の空気袋81は、対向するシート部材86同士を外周縁に位置する溶着部81aよりも小さい四辺枠状にブリッジ溶着し、このブリッジ溶着部81bで複数の開口を囲うことで、隣り合う空気袋81を一体に形成し、そして、ブリッジ溶着部81bの内側で流体的に連続させる。ここで、ブリッジ溶着及びブリッジ溶着部のブリッジとは、隣り合う空気袋81を一体に接合することを意味する。
被接合部82は、カーラ5と隣接して配置される空気袋81の縁部の少なくとも一部に、単数又は複数設けられる。被接合部82は、空気袋81を構成するシート部材86の一部によって形成される。
本実施形態においては、被接合部82は、図7乃至図9、図13乃至図15に示すように、空気袋81の短手方向の縁部のそれぞれに一つずつ設けられる例を用いて説明する。なお、例えば、被接合部82は、スリットにより空気袋81の長手方向に分割されていてもよく、また、空気袋81の長手方向に複数設けられていてもよい。被接合部82は、押圧カフ71がカーラ5の内周面に配置されたときに、少なくとも、カーラ5の外周面に接合される。また、例えば、二つの被接合部82は、積層され、そして溶着される。
なお、二つの被接合部82は、例えば、空気袋81の短手方向の長さが異なる長さに設定される。この例においては、二つの被接合部82は、カーラ5の短手方向の一端側において積層されて溶着される。なお、二つの被接合部82は、先端がカーラ5の外周面に配置可能であれば、その長さは適宜設定可能であり、積層可能であってもなくてもよいが、積層可能な長さに設定される場合には、先端がカーラ5の外周面の外縁よりも外方に延設されない長さが好ましい。
流路体83は、図7、図13乃至図17に示すように、一つの空気袋81、例えば、カーラ5に隣接する空気袋81の長手方向で一端の縁部の一部に一体に設けられる。具体例として、流路体83は、空気袋81の装置本体3に近い端部に設けられる。また、流路体83は、空気袋81の短手方向の幅よりも小さい幅で一方向に長い形状に形成され、先端が円形状に形成される。流路体83は、先端に接続部84を有する。流路体83は、接続部84を介して流路部15に接続され、装置本体3の流路部15と空気袋81との間の流路を構成する。
流路体83は、二枚のシート部材86に接続部84を配置した状態で、シート部材86の空気袋81を構成する領域に隣接するシート部材86の一部を一方向に長い枠状に熱により溶着することで構成される。このような流路体83は、カーラ5の内周面及び引張カフ74の間に配置され、先端がカーラ5のカバー部5aが設けられた領域の手首200側の主面であって、且つ、第1孔部5f1と対向する位置に配置される。
なお、流路体83が設けられる空気袋81は、二枚のシート部材86を矩形枠状に溶着する溶着部81aの一部を非溶着とし、流路体83を構成する溶着部83aと連続する構成とすることで、空気袋81が流路体83に流体的に連続する。
接続部84は、例えばニップルである。接続部84は、流路体83の先端に設けられる。接続部84の先端は、流路体83を構成する二枚のシート部材86のうち、カーラ5と対向するシート部材86から露出する。接続部84は、カバー部5aの第1孔部5f1に挿通され、流路部15に接続される。
このような構成を有する押圧カフ71は、具体例として、図8、図9及び図52に示すように、手首200側から、第1シート部材86aと、第1シート部材86aと一層目の空気袋81を構成する第2シート部材86bと、第2シート部材86bと一体に接合されるとともに、被接合部82を構成する第3シート部材86cと、第3シート部材86cと二層目の空気袋81及び流路体83を構成する第4シート部材86dと、を備える。なお、押圧カフ71は、隣り合うシート部材86が熱による溶着により接合されることで一体に構成される。
第1シート部材86a及び第2シート部材86bは、空気袋81と同様の矩形状に構成され、四辺の周縁部が溶着されることで空気袋81を構成する。第2シート部材86b及び第3シート部材86cは、対向して配置され、それぞれ、二つの空気袋81を流体的に連続させる複数の開口86b1、86c1を有する。また、第2シート部材86b及び第3シート部材86cは、複数の開口86b1、86c1の周囲を、空気袋81を溶着した四辺よりも小さい四辺枠状に熱によりブリッジ溶着されることで、一体に接合される。
第3シート部材86cは、例えば、空気袋81、被接合部82及び流路体83を構成可能な形状に構成される。第4シート部材86dは、例えば、空気袋81及び流路体83を構成可能な形状に構成される。また、第4シート部材86dは、例えば、接続部84の先端を挿入可能な孔部86d1を有する。
第3シート部材86c及び第4シート部材86dは、対向して配置され、空気袋81及び流路体83が流体的に連続するように、空気袋81及び流路体83の周縁形状に沿って熱により溶着され、所定の形状に裁断されることで空気袋81、被接合部82及び流路体83を構成する。
第4シート部材86dの孔部86d1に接続部84が配置され、孔部86d1の周囲が接続部84と熱により溶着される。さらに、第4シート部材86dはカーラ5の内周面に、第3シート部材86cの被接合部82はカーラ5の外周面に、それぞれ接合層75を介して接合される。
背板72は、図8、図9及び図52に示すように、接合層75により押圧カフ71の第1シート部材86aの外面に貼付される。背板72は、樹脂材料で板状に形成される。背板72は、例えば、ポリプロピレンからなり、厚さが1mm程度の板状に形成される。背板72は、形状追従性を有する。
ここで、形状追従性とは、配置される手首200の被接触箇所の形状を倣うように背板72が変形可能な機能をいい、手首200の被接触箇所とは、背板72が対向する手首200の領域をいう。ここでの接触とは、直接的な接触及びセンシングカフ73を介した間接的な接触の双方を含む。
例えば、図9に示すように、背板72は、その両主面に長手方向に対して直交する方向に延びる複数の溝72aを有する。複数の溝72aは、背板72の厚さ方向においてそれぞれ対向する。また、複数の溝72aは、背板72の長手方向に等間隔に配置される。
背板72は、複数の溝72aを有する部位が溝72aを有さない部位に比べて薄肉となることで、複数の溝72aを有する部位が変形しやすいことから、手首200の形状に倣って変形し、手首の周方向に延在する形状追従性を有する。背板72は、手首200の手の平側を覆う長さに形成される。背板72は、手首200の形状に沿った状態で、押圧カフ71からの押圧力をセンシングカフ73の背板72側の主面に伝達する。
センシングカフ73は、流路部15を介してポンプ14に流体的に接続される。センシングカフ73は、背板72の手首200側の主面に固定される。センシングカフ73は、図4及び図52に示すように、手首200の動脈210が存する領域に例えば直接接触する。ここで、動脈210とは、橈骨動脈及び尺骨動脈である。センシングカフ73は、背板72の長手方向及び幅方向で、背板72と同一形状か、又は、背板72よりも小さい形状に形成される。センシングカフ73は、膨張することで手首200の手の平側の動脈210が存する領域を圧迫する。センシングカフ73は、膨張した押圧カフ71により、背板72を介して手首200側に押圧される。
具体例として、センシングカフ73は、図8、図9、図13、図14、図17及び図18に示すように、一つの空気袋(第2袋状構造体)91と、空気袋91と連通する流路体92と、流路体92の先端に設けられた接続部93と、少なくとも一部が押圧カフ71に接合される接合代94と、を含む。センシングカフ73は、空気袋91の一方の主面が背板72に固定される。例えば、センシングカフ73は、背板72の手首200側の主面に接合層75により接合される。このようなセンシングカフ73は、二枚のシート部材96を一体に溶着することで構成される。
ここで、空気袋91とは、袋状構造体であり、本実施形態においては血圧測定装置1がポンプ14により空気を用いる構成であることから、空気袋を用いて説明するが、空気以外の流体を用いる場合には、袋状構造体は液体袋等であってもよい。
空気袋91は、一方向に長い矩形状に構成される。空気袋91は、例えば、二枚のシート部材96を組み合わせ、図8、図9、図13、図14、図17及び図18に溶着部91aを示すように、一方向に長い矩形枠状に熱により溶着することで構成される。
流路体92は、空気袋91の長手方向で一端の縁部の一部に一体に設けられる。具体例として、流路体92は、空気袋91の装置本体3に近い端部に設けられる。また、流路体92は、空気袋91の短手方向の幅よりも小さい幅で一方向に長い形状に形成され、先端が円形状に形成される。流路体92は、先端に接続部93を有する。流路体92は、先端に、接続部93を有する。流路体92は、接続部93を介して流路部15に接続され、装置本体3の流路部15と空気袋91との間の流路を構成する。
流路体92は、二枚のシート部材96に接続部93を配置した状態で、シート部材96の空気袋91を構成する領域に隣接するシート部材96の一部を一方向に長い枠状に熱により溶着することで構成される。なお、空気袋91は、二枚のシート部材96を矩形枠状に溶着する溶着部91aの一部を非溶着とし、流路体92を構成する溶着部92aと連続する構成とすることで、空気袋91及び流路体92を流体的に連続する。このような流路体92は、カーラ5の内周面及び引張カフ74の間に配置され、先端がカーラ5のカバー部5aが設けられた領域の手首200側の主面であって、且つ、第2孔部5f2と対向する位置に配置される。
接続部93は、例えばニップルである。接続部93は、流路体92の先端に設けられる。また、接続部93の先端は、流路体92を構成する二枚のシート部材96のうち、カーラ5及び背板72と対向するシート部材96から外部に露出する。接続部93は、カバー部5aの第2孔部5f2に挿通され、流路部15に接続される。
接合代94は、押圧カフ71の複数の空気袋81のうち空気袋91に隣接する空気袋81、換言すると、背板72側の空気袋81の溶着部81aの一部に溶着により接合可能に形成されており、具体例として、背板72側の空気袋81の長手方向に沿う外縁部に、接合される。
空気袋81の外縁部は、空気袋81の外縁の周囲の領域である。本実施形態では、空気袋81は、2枚のシート部材86が溶着されることで構成されることから、溶着部81aは、空気袋81の外縁部の一例である。
図17に示すように、接合代94は、例えば、空気袋91の溶着部91a、及び流路体92の溶着部92aの一部に連続して一体に形成される。この為、接合代94は、その一部が空気袋91の長手方向に沿う外縁部に形成される。接合代94は、例えば、二枚のシート部材96の、空気袋91を構成する領域、及び流路体92を構成する領域に隣接する領域を、押圧カフ71の背板72側の空気袋81及び溶着部81aと同形状に形成することで、構成される。
図13に示すように、接合代94の外縁部は、押圧カフ71の背板72側の空気袋81の溶着部81aと同形状に形成される。接合代94の外縁部のうち、空気袋81の長手方向に沿う溶着部81aと対向する部分は、溶着部81aに溶着される接合部94aを構成する。接合部94aは、溶着により、押圧カフ71に接合される。換言すると、接合代94の、センシングカフ73の空気袋91の長手方向に沿う2つの外縁部が、空気袋81の長手方向に沿う溶着部81aの一端から他端まで接合されている。接合代94の短手方向に沿う外縁部は、空気袋81の短手方向に沿う溶着部81aには接合されない。
このような構成を有するセンシングカフ73は、具体例として、図8及び図9に示すように、手首200側から第5シート部材96a及び第6シート部材96bを備える。なお、センシングカフ73は、隣り合うシート部材96が熱による溶着により接合されることで構成される。
例えば、第5シート部材96a及び第6シート部材96bは、空気袋91、流路体92及び接合代94を構成可能な形状に構成される。第5シート部材96a及び第6シート部材96bは、対向して配置され、空気袋91及び流路体92が流体的に連続するように、空気袋91及び流路体92の周縁形状に沿って熱により溶着され、所定の形状に裁断されることで空気袋91、流路体92及び接合代94を構成する。
また、第6シート部材96bは、例えば、接続部93の先端を挿入可能な孔部96b1を有する。孔部96b1に接続部93が配置され、孔部96b1の周囲が接続部93と熱により溶着される。第6シート部材96bは、背板72の内周面に、接合層75を介して接合される。
図19に示すように、押圧カフ71、背板72、及びセンシングカフ73は、押圧カフ71及びセンシングカフ73が固定され、背板72が押圧カフ71及びセンシングカフ73に固定されることで、一体に構成され、カフユニット250を構成する。カフユニット250は、後述する、曲面に構成される載置面401を有する冶具400を用いて製造されることで、カーラ5に接合される前の状態で、カーラ5の押圧カフ71が接合される面に倣って湾曲した形状に構成される。
引張カフ74は、流路部15を介してポンプ14に流体的に接続される。図4に示すように、引張カフ74は、膨張することで手首200から離間するようにカーラ5を押圧することで、ベルト4及びカーラ5を手首200の手の甲側に引っ張る。引張カフ74は、図10、図11、図20及び図21に示すように、複数の、例えば六層の空気袋101と、カーラ5と対向する空気袋101に設けられた被接合部102と、カーラ5と対向する空気袋101に設けられた接続部103と、少なくともカーラ5と対向する空気袋101に設けられた切欠部104と、を含む。このような引張カフ74は、複数のシート部材106を一体に溶着することで構成される。また、引張カフ74は、流路体83、92が設けられた領域、及び、カバー部5aを含むカーラ5の手首200の手の甲側に固定される。即ち、カーラ5の手首200の手の甲側及び引張カフ74の間に、押圧カフ71の流路体83及びセンシングカフ73の流路体92が配置される。
また、引張カフ74は、膨張方向、本実施形態においては、カーラ5及び手首200の対向する方向で、膨張時の厚さが、押圧カフ71の膨張方向における膨張時の厚さ、及び、センシングカフ73の膨張方向における膨張時の厚さよりも厚く構成される。即ち、引張カフ74の空気袋101は、押圧カフ71の空気袋81及びセンシングカフ73の空気袋91よりも多い層構造を有し、カーラ5から手首200に向かって膨張したときの厚さが押圧カフ71及びセンシングカフ73よりも厚い。
本実施形態において、六層の空気袋101を含む引張カフ74は、図10、図11及び図20に示すように、一つの空気袋101により構成される第1外層111、第1外層111に熱により溶着して一体に組み合わされた二層の空気袋101により構成される第1中間層112、第1中間層112に熱により溶着して一体に組み合わされた二層の空気袋101により構成される第2中間層113、及び、第2中間層113に熱により溶着して一体に組み合わされた一つの空気袋101により構成される第2外層114を備える。
ここで、空気袋101とは、袋状構造体であり、本実施形態においては血圧測定装置1がポンプ14により空気を用いる構成であることから、空気袋を用いて説明するが、空気以外の流体を用いる場合には、袋状構造体は当該流体により膨張する流体袋であればよい。複数の空気袋101は、積層され、積層方向に流体的に連通する。
空気袋101は、一方向に長い矩形状の袋形状に形成される。また、空気袋101は、短手方向の幅が、カーラ5の短手方向の幅と同じ幅に設定される。空気袋101は、例えば、二枚のシート部材106を組み合わせ、図10、図11、図13、図14、図20及び図21に溶着部101aを示すように、一方向に長い矩形枠状に熱により溶着することで構成される。六層の空気袋101は、互いに対向するシート部材106に設けられた開口によって流体的に連続する。
また、六層の空気袋101は、第1外層111及び第1中間層112、第1中間層112及び第2中間層113、並びに、第2中間層113及び第2外層114がそれぞれ対向するシート部材106同士を外周縁に位置する溶着部81aよりも小さい四辺枠状にブリッジ溶着し、このブリッジ溶着部101bで複数の開口を囲うことで、隣り合う空気袋101を一体に形成し、そして、ブリッジ溶着部101bの内側で流体的に連続させる。
第1外層111は、手首200側に配置される一つの空気袋101により形成される。第1外層111は、六層の空気袋101のうち、手首200側から第一層の空気袋101を構成する。
第1中間層112は、第1外層111に積層される。第1中間層112は、二層の空気袋101により形成される。第1中間層112は、六層の空気袋101のうち、手首200側から第二層及び第三層の空気袋101を構成する。第1中間層112は、二層の空気袋101が外周縁で一体に溶着されることで構成される。換言すると、第1中間層112は、4枚のシート部材106を空気袋101の外周縁形状で一体に溶着することで形成される。
第2中間層113は、第1中間層112に積層される。第2中間層113は、二層の空気袋101により形成される。第2中間層113は、六層の空気袋101のうち、手首200側から第四層及び第五層の空気袋101を構成する。第2中間層113は、二層の空気袋101が外周縁で一体に溶着されることで構成される。換言すると、第2中間層113は、4枚のシート部材106を空気袋101の外周縁形状で一体に溶着することで形成される。
第2外層114は、カーラ5側に配置される一つの空気袋101により形成される。第2外層114は、六層の空気袋101のうち、手首200側から第六層の空気袋101を構成する。
被接合部102は、カーラ5と隣接して配置される空気袋101の縁部の少なくとも一部に、単数又は複数設けられる。被接合部102は、空気袋101を構成するシート部材106の一部によって形成される。
本実施形態においては、被接合部102は、空気袋101の短手方向の縁部のそれぞれに、空気袋101の長手方向で二つずつ設けられる例を用いて説明する。なお、例えば、被接合部102は、カーラ5のカバー部5aと対向する位置を避けて空気袋101に設けられる。また、例えば、被接合部102は、カーラ5に設けられた給電部8の後述する給電端子8bと対向する部位に、給電端子8bを外部に露出させるための逃げ部102aを有する。逃げ部102aは、例えば、給電端子8bを外部に露出可能な開口であり、一例として円形状である。
被接合部102は、引張カフ74がカーラ5の内周面に配置されたときに、少なくとも、カーラ5の外周面に接合される。また、空気袋101の短手方向で同じ位置に配置される被接合部102は、積層され、そして溶着される。
なお、二つの被接合部102は、例えば、空気袋101の短手方向の長さが異なる長さに設定される。この例においては、二つの被接合部102は、カーラ5の短手方向の一端側において積層されて溶着される。なお、二つの被接合部102は、先端がカーラ5の外周面に配置可能であれば、その長さは適宜設定可能であり、積層可能であってもなくてもよいが、積層可能な長さに設定される場合には、先端がカーラ5の外周面の外縁よりも外方に延設されない長さが好ましい。
接続部103は、例えばニップルである。接続部103は、カーラ5と隣接して配置される空気袋101の長手方向で中央側であって、且つ、カバー部5aの第3孔部5f3と対向する位置に設けられる。接続部103の先端は、空気袋101を構成する二枚のシート部材106のうち、カーラ5と対向するシート部材106から露出する。接続部103は、カバー部5aの第3孔部5f3に挿通され、流路部15に接続される。
切欠部104は、図19に示すように、カーラ5に設けられた逃げ部5bと対向する位置に設けられる。切欠部104は、第2外層114を形成する第六層の空気袋101に設けられる。
具体例として、引張カフ74は、図10、図11及び図20に示すように、手首200側から、第7シート部材106aと、第8シート部材106bと、第9シート部材106cと、第10シート部材106dと、第11シート部材106eと、第12シート部材106fと、第13シート部材106gと、第14シート部材106hと、第15シート部材106iと、第16シート部材106jと、第17シート部材106kと、第18シート部材106lと、を備えている。なお、引張カフ74は、隣り合うシート部材106が熱による溶着により接合されることで一体に構成される。
第7シート部材106a乃至第18シート部材106lは、空気袋101と同様の矩形状に構成される。第7シート部材106a及び第8シート部材106bは、空気袋101の四辺の周縁部形状に沿って熱により溶着されることで、手首200側から一層目の空気袋101を構成する。即ち、第7シート部材106a及び第8シート部材106bは、第1外層111を構成する。
第8シート部材106b及び第9シート部材106cは、対向して配置され、それぞれ、二つの空気袋101を流体的に連続させる複数の開口106b1、106c1を有する。また、第8シート部材106b及び第9シート部材106cは、複数の開口106b1、106c1の周囲を、空気袋101を溶着した四辺よりも小さい四辺枠状に熱によりブリッジ溶着されることで、一体に接合される。
第9シート部材106c及び第10シート部材106dは、空気袋101の四辺の周縁部形状に沿って熱により溶着されることで、手首200側から二層目の空気袋101を構成する。
第10シート部材106d及び第11シート部材106eは、図10及び図11及び図20に示すように、対向して配置され、それぞれ、二つの空気袋101を流体的に連続させる複数の開口106d1、106e1を有する。第11シート部材106e及び第12シート部材106fは、空気袋101の四辺の周縁部形状に沿って熱により溶着されることで、手首200側から三層目の空気袋101を構成する。
なお、第9シート部材106c、第10シート部材106d、第11シート部材106e及び第12シート部材106fは、空気袋101の四辺の周縁部形状に沿って熱により一体に溶着されることで、第二層及び第三層の空気袋101が一体に形成された第1中間層112を構成する。
第12シート部材106f及び第13シート部材106gは、図10、図11及び図20に示すように、対向して配置され、それぞれ、二つの空気袋101を流体的に連続させる複数の開口106f1、106g1を有する。また、第12シート部材106f及び第13シート部材106gは、複数の開口106f1、106g1の周囲を、空気袋101を溶着した四辺よりも小さい四辺枠状に熱によりブリッジ溶着されることで、一体に接合される。
第13シート部材106g及び第14シート部材106hは、空気袋101の四辺の周縁部形状に沿って熱により溶着されることで、手首200側から四層目の空気袋101を構成する。
第14シート部材106h及び第15シート部材106iは、図10、図11及び図21に示すように、対向して配置され、それぞれ、二つの空気袋101を流体的に連続させる複数の開口106h1、106i1を有する。第15シート部材106i及び第16シート部材106jは、空気袋101の四辺の周縁部形状に沿って熱により溶着されることで、手首200側から五層目の空気袋101を構成する。
なお、第13シート部材106g、第14シート部材106h、第15シート部材106i及び第16シート部材106jは、空気袋101の四辺の周縁部形状に沿って熱により一体に溶着されることで、第四層及び第五層の空気袋101が一体に形成された第2中間層113を構成する。
第16シート部材106j及び第17シート部材106kは、図10、図11及び図21に示すように、対向して配置され、それぞれ、二つの空気袋101を流体的に連続させる複数の開口106j1、106k1を有する。また、第17シート部材106kは、例えば、空気袋101及び被接合部102を構成可能な形状に構成される。第16シート部材106j及び第17シート部材106kは、複数の開口106j1、106k1の周囲を、空気袋101を溶着した四辺よりも小さい四辺枠状に熱によりブリッジ溶着されることで、一体に接合される。
第17シート部材106k及び第18シート部材106lは、空気袋101の四辺の周縁部形状に沿って熱により溶着され、所定の形状に裁断されることで、手首200側から六層目の切欠部104を有する空気袋101及び被接合部102を構成する。
また、第18シート部材106lは、例えば、接続部103の先端を挿入可能な孔部106l1を有する。第18シート部材106lは、孔部106l1に接続部103が配置され、そして、孔部106l1の周囲が接続部103と熱により溶着される。また、第18シート部材106lは、カーラ5の内周面に、第17シート部材106kの被接合部102はカーラ5の外周面に、それぞれ接合層75を介して接合される。
また、押圧カフ71、センシングカフ73及び引張カフ74を形成する各シート部材86、96、106は、例えば、0.15mmの厚さに形成される。各シート部材86、96、106は、熱可塑性樹脂材料により形成される。熱可塑性樹脂材料は、熱可塑性エラストマーである。シート部材86、96、106を構成する熱可塑性樹脂材料としては、例えば、熱可塑性ポリウレタン系樹脂(Thermoplastic PolyUrethane、以下TPUと表記する)、塩化ビニル樹脂(PolyVinyl Chloride)、エチレン酢酸ビニル樹脂(Ethylene-Vinyl Acetate)、熱可塑性ポリスチレン系樹脂(Thermoplastic PolyStyrene)、熱可塑性ポリオレフィン樹脂(Thermoplastic PolyOlefin)、熱可塑性ポリエステル系樹脂(ThermoPlastic Polyester)及び熱可塑性ポリアミド樹脂(Thermoplastic PolyAmide)を用いることができる。なお、押圧カフ71、センシングカフ73は、少なくとも空気袋81、101を構成する複数のシート部材86、106のうち、少なくともカーラ5と溶着されるシート部材86、106がカーラ5と同種材料で構成される。
例えば、シート部材86、96、106は、Tダイ押し出し成形や射出成形等の成形方式が用いられる。シート部材86、96、106は、各成形方式で成形された後、所定の形状にサイジングされ、そして、サイジングした個片を溶着等により接合することで袋状構造体81、91、101を構成する。溶着の方式としては、高周波ウェルダーやレーザー溶着が用いられる。
流体回路7は、ケース11、ポンプ14、流路部15、開閉弁16、圧力センサ17、押圧カフ71、センシングカフ73、及び、引張カフ74によって構成される。以下、流体回路7の具体例を説明する。
流体回路7は、図5に示すように、例えば、第1開閉弁16Aを介してポンプ14とセンシングカフ73、第1圧力センサ17A及び第2圧力センサ17Bとを連続する第1流路7aと、ポンプ14及び第1開閉弁16Aの間の第1流路7aから分岐されることで構成され、第2開閉弁16B、第3開閉弁16C及び第4開閉弁16Dを順次介してポンプ14と大気とを連続する第2流路7bと、第2流路7bの第2開閉弁16B及び第3開閉弁16C間の中途部が分岐されることで構成され、ポンプ14から引張カフ74を連続する第3流路7cと、第2流路7bの第3開閉弁16C及び第4開閉弁16D間の中途部が分岐されることで構成され、ポンプ14から押圧カフ71を連続する第4流路7dと、を備えている。
このような流体回路7は、第2開閉弁16B及び第3開閉弁16Cが開き、第1開閉弁16A及び第4開閉弁16Dが閉じることで、第2流路7bから分岐する第3流路7c及び第4流路7dがポンプ14と接続し、ポンプ14、押圧カフ71及び引張カフが流体的に接続される。
流体回路7は、第1開閉弁16A、第2開閉弁16B及び第3開閉弁16Cが開き、そして、第4開閉弁16Dが閉じることで、第1流路7a、第2流路7bから分岐する第3流路7c及び第4流路7dがポンプ14と接続され、ポンプ14、押圧カフ71及び引張カフ、並びに、ポンプ14及びセンシングカフ73が流体的に接続される。流体回路7は、第2開閉弁16B、第3開閉弁16C及び第4開閉弁16Dが開き、そして、第1開閉弁16Aが閉じることで、第2流路7b、第3流路7c及び第4流路7dがポンプ14と接続され、ポンプ14、押圧カフ71、引張カフ74及び大気が流体的に接続される。また、流体回路7は、第1開閉弁16A、第2開閉弁16B、第3開閉弁16C及び第4開閉弁16Dが開くことで、第1流路7a、第2流路7b、第3流路7c及び第4流路7dがポンプ14と接続され、ポンプ14、押圧カフ71、センシングカフ73、引張カフ74及び大気が流体的に接続される。
給電部8は、図6及び図7に示すように、装置本体3から突出するカーラ5の一端側の外面に形成された窪み5cに設けられる。例えば、給電部8は、充電器の充電ケーブルに設けられたコネクタと接続可能に構成される。
図3、図6及び図7に示すように、給電部8は、配線部8aと、給電端子8bと、カーラ5の窪み5cに配置された配線部8aを覆うカバー8cと、を備えている。配線部8aは、一端が給電端子8bに、他端が制御部55に接続される。給電端子8bは、例えば二つの円形状の端子により構成される。例えば、配線部8a及び給電端子8bは、ポリイミド等のベースフィルムに導電性金属膜等が設けられたFPC(Flexible printed circuits)等により形成される。カバー8cは、窪み5cと同形状に形成され、窪み5cを覆うとともに、窪み5cに設けられたときに、上面が、カーラ5の短手側の外面と面一となる。
次に、カフユニット250の一部を構成する第1構造体251の製造方法の一例について、図22乃至図33を用いて以下説明する。
先ず、図33に示すように、押圧カフ71を構成する複数のシートを溶着して一体化した第1構造体251を構成する。
第1構造体251の製造では、先ず、材料を裁断し(ステップST11)、所定の形状のシートを形成する。なお、ここで、所定の形状とは、空気袋81及び被接合部82の形状に加え、溶着代や各加工機に位置合わせを行う位置合わせ用のダミー部等を含む形状である。具体例として、プレス機によって、熱可塑性樹脂材料で形成されたシート状の材料から、図23乃至図26に示すように、第1シート86A、第2シート86B、第3シート86C及び第4シート86Dをそれぞれ打ち抜く。
図23に示すように、第1シート86Aは、位置決めピン301を挿入可能な位置決めピン用孔71aを有し、空気袋81の外周縁形状よりも大きい矩形状のシート部材である。第1シート86Aは、第1シート部材86aを形成する。ピン用孔71aは、複数、具体例として2つ形成されている。2つのピン用孔71aは、第1シート86Aの空気袋81を構成する領域を挟んで空気袋81の長手方向で両側のそれぞれに1つずつ配置される。
図24に示すように、第2シート86Bは、位置決めピン301を挿入可能な位置決めピン用孔71a、及び、隣接する空気袋81を流体的に連通する開口を有し、空気袋81の外周縁形状よりも大きい矩形状のシート部材である。第2シート86Bは、第2シート部材86bを形成する。ピン用孔71aは、複数、具体例として2つ形成されている。ピン用孔71aは、第2シート86Bの空気袋81を構成する領域を挟んで空気袋81の長手方向で両側のそれぞれに1つずつ配置される。また、ここで、第2シート86Bの開口は、第2シート部材86bの開口86b1を構成する。
図25に示すように、第3シート86Cは、位置決めピン301を挿入可能な位置決めピン用孔71a、及び、隣接する空気袋81を流体的に連通する開口を有し、空気袋81及び被接合部82の外周縁形状よりも大きい矩形状のシート部材である。第3シート86Cは、第3シート部材86cを形成する。ピン用孔71aは、複数、具体例として2つ形成されている。ピン用孔71aは、第3シート86Cの空気袋81を構成する領域を挟んで空気袋81の長手方向で両側のそれぞれに1つずつ配置される。ここで、第3シート86Cの開口は、第3シート部材86cの開口86c1を構成する。
第4シート86Dは、位置決めピン301を挿入可能な位置決めピン用孔71a、及び、接続部84を挿入する孔部86d1を有し、空気袋81及び被接合部82の外周縁形状よりも大きい矩形状のシート部材である。第4シート86Dは、第4シート部材86dを形成する。ピン用孔71aは、複数、具体例として2つ形成されている。ピン用孔71aは、第4シート86Dの空気袋81を構成する領域を挟んで空気袋81の長手方向で両側のそれぞれに1つずつ配置される。
次に、図22に示すように、第4シート86Dに接続部84を溶着する(ステップST12)。具体例として、第4シート86Dに設けられた孔部86d1に接続部84を差し込み、高周波溶着機によって、接続部84を第4シート86Dに溶着する。
次に、図22、図27及び図28に示すように、第2シート86B及び第3シート86Cをブリッジ溶着する(ステップST13)。具体的には、第2シート86B及び第3シート86Cを積層させて、第2シート86B及び第3シート86Cのそれぞれの位置決めピン用孔71aを位置決めピン301に配置し、下金型302に第2シート86B及び第3シート86Cを配置する。これによりシート86B、86Cが、下金型302に対して位置決めされる。なお、下金型302には、電極を構成する突起である電極部302aが設けられる。また、電極部302aは、第2シート86B及び第3シート86Cを溶着する領域に当接可能な形状に形成されており、この工程で用いられる電極部302aは、端面がブリッジ溶着部81bの形状に形成された突起である。
そして、高周波溶着機によって、空気袋81の外周縁形状よりも小さい矩形枠状にブリッジ溶着して、ブリッジ溶着部81bを形成し、第2シート86B及び第3シート86Cを一体に溶着する。
次に、図29及び図30に示すように、第2シート86Bに第1シート86Aを溶着する。具体的には、ステップST13でブリッジ溶着した第2シート86B及び第3シート86C、並びに第1シート86Aのそれぞれの位置決めピン用孔71aを位置決めピン301に配置し、下金型302にブリッジ溶着した第2シート86B及び第3シート86C、並びに第1シート86Aを配置する。これにより、シート86A、86B、86Cは、下金型302に位置決めされる。なお、この工程で用いられる下金型302の電極部302aは、端面が溶着部81aの形状に形成された突起である。
このとき、図29に示すように、下金型302に設けられた空洞302bに下金型302側に配置される第3シート86Cの少なくとも第2シート86B及び第1シート86Aを溶着する部位と対向する部位を逃がす。そして、高周波溶着機によって、空気袋81の外周縁形状に溶着して、溶着部81aを形成する。
次に、溶着により一体化された第2シート86B、第3シート86C及び第1シート86Aと、第4シート86Dと、を溶着する。具体的には、図31及び図32に示すように、溶着により一体化された第2シート86B、第3シート86C、及び第1シート86Aと、第4シート86Dと、のそれぞれの位置決めピン用孔71aを位置決めピン301に配置し、下金型302に溶着により一体化された第2シート86B、第3シート86C、及び第1シート86A、並びに第4シート86Dを配置する。ここで言う、溶着により一体化された第2シート86B、第3シート86C、及び第1シート86Aとは、図27及び図28に示すようにブリッジ溶着により一体化された第2シート86B及び第3シート86Cと、図29及び図30に示すように溶着部81aで溶着された第1シート86Aと、である。なお、この工程で用いられる下金型302の電極部302aは、端面が溶着部81a及び溶着部83aの形状に形成された突起である。すなわち、電極部302aの端面の形状は、空気袋81及び流路体83を構成可能な形状である。
また、このとき、図31に示すように、下金型302に設けられた空洞302bに第1シート86A及び第2シート86Bの少なくとも第3シート86C及び第4シート86Dを溶着する部位と対向する部位を逃がす。そして、高周波溶着機によって、空気袋81の外周縁形状及び流路体83の外周縁形状に溶着して、溶着部81a及び溶着部83aを形成する。これらの工程により、第1構造体251が製造される。
次に、図38に示すように、カフユニット250の一部である、センシングカフ73を構成する複数のシートを溶着して一体化した第2構造体252を構成する。なお、本実施形態では、一例として、第1構造体251を製造した後に第2構造体252が製造される例が説明されるが、第1構造体251、及び第2構造体252の製造の順番は、限定されない。第1構造体251及び第2構造体252は、並行して製造されてもよい。
第2構造体252の製造では、図34に示すように、先ず、材料を裁断し(ステップST21)、所定の形状のシートを形成する。なお、ここで、所定の形状とは、空気袋91及び流路体92の形状に加え、溶着代や各加工機に位置合わせを行う位置合わせ用のダミー部等を含む形状である。具体例として、プレス機によって、熱可塑性樹脂材料で形成されたシート状の材料から、図35及び図36に示すように、第5シート96A及び第6シート96Bをそれぞれ打ち抜く。
図35に示すように、第5シート96Aは、位置決めピン321を挿入可能な位置決めピン用孔73aを有し、空気袋91及び流路体92の外周縁形状よりも大きい矩形状のシート部材である。第5シート96Aは、第5シート部材96aを形成する。ピン用孔73aは、複数、具体例として2つ形成されている。2つのピン用孔73aは、第5シート96Aの空気袋91を構成する領域を挟んで空気袋91の長手方向で両側のそれぞれに1つずつ配置される。
図36に示すように、第6シート96Bは、位置決めピン321を挿入可能な位置決めピン用孔73a、及び、接続部93を挿入する孔部96b1を有し、空気袋91及び流路体92の外周縁形状よりも大きい矩形状のシート部材である。第6シート96Bは、第6シート部材96bを形成する。ピン用孔73aは、複数、具体例として2つ形成されている。2つのピン用孔73aは、第6シート96Bの空気袋91を構成する領域を挟んで空気袋91の長手方向で両側のそれぞれに1つずつ配置される。
次に、図34に示すように、第6シート96Bに接続部93を溶着する(ステップST22)。具体例として、第6シート96Bに設けられた孔部96b1に接続部93を差し込み、高周波溶着機によって、接続部93を第6シート96Bに溶着する。
次に、図37及び図38に示すように、第5シート96A及び第6シート96Bを溶着する。具体的には、第5シート96A及び第6シート96Bのそれぞれの位置決めピン用孔73aを位置決めピン321に配置し、下金型320に第5シート96A及び第6シート96Bを配置する。これにより、下金型320に対して、第5シート96A及び第6シート96Bが位置決めされる。なお、この工程で用いられる下金型320の電極部322は、端面が空気袋91の溶着部91a及び流路体92の溶着部92aの形状に形成された突起である。そして、高周波溶着機によって、空気袋91の外周縁形状、及び流路体92の外周形状に溶着して、溶着部81a、91aを形成する。これらの工程により、第2構造体252が製造される。
次に、第1構造体251、第2構造体252、及び背板72からカフユニット250を製造する製造法の一例を、図39乃至図43を用いて説明する。
先ず、図39に示すように、第1の固定を行う(ステップST31)。第1の固定では、第1構造体251及び背板72を固定する。具体的には、まず、背板72を、湾曲する冶具に配置し、加熱炉で加熱することで熱加工し、所定の形状に湾曲させる。ここで言う所定の形状は、カーラ5の、押圧カフ71を介して背板72が対向する面に沿う形状である。次に、図41に示すように、冶具400に第1構造体251をセットする。
冶具400は、図40に示すように、載置面401と、位置決め用の位置決めピン402と、を有する。載置面401は、カーラ5の、押圧カフ71が配置される面に対応する曲面に形成される。載置面401は、少なくとも、空気袋81の全域と、空気袋91の全域を配置可能な大きさを有する。ここで配置可能とは、平面視で、載置面401と重なる位置に配置されることである。すなわち、載置面401に直接接触することで載置面401に沿って湾曲可能であり、第2構造体252においては、直接または第1構造体251及び背板72の少なくとも一方を介して間接的に載置面401に接触することで載置面401に沿って湾曲可能となる位置に配置されることである。
本実施形態では、一例として、ピン402がピン用孔71a、73aにセットされた状態で、載置面401は、空気袋81の全域と、流路体83の一部とを配置可能であり、かつ、空気袋91の全域と、流路体92の一部と、を配置可能な大きさを有する。
ここで言う、カーラ5の、押圧カフ71が配置される面に対応する曲面とは、当該曲面に沿って形成されるカフユニット250をカーラ5に固定したときに、カフユニット250がカーラ5に固定する前に比較して湾曲することで押圧カフ71及びセンシングカフ73の少なくとも一方に、膨張を阻害するしわが発生することを抑制できる曲面である。載置面401は、例えば、カーラ5の、押圧カフ71が配置される面と同じ曲率を有する曲面である。他の例では、載置面401は、カーラ5の、押圧カフ71が配置される面と略同じ曲率を有する曲面である。
位置決め用の位置決めピン402は、複数、具体例として2つ形成される。位置決めピン402は、第1構造体251の各ピン用孔71a、及び第2構造体252の各ピン用孔73aに配置可能に構成される。また、位置決め用の位置決めピン402は、冶具400に対する第1構造体251及び第2構造体252の移動を防止可能な形状、具体例として、ピン用孔71a、73aに嵌る形状に形成される。一方の位置決めピン402は、載置面401の例えば一端に配置される。他方のピン402は、載置面401の例えば他端に配置される。
第1構造体251は、位置決め用の位置決めピン402にセットされる。具体例として、第1構造体251の一方のピン用孔71aに一方の位置決めピン402を配置し、他方のピン用孔71aに他方の位置決めピン402を配置する。ここで言う一方のピン用孔71aは、シート86A、86B、86C、86Dのそれぞれの2つのピン用孔71aのうち、対向配置される一方のピン用孔71aである。他方のピン用孔71aは、対向配置される他方のピン用孔71aである。次に、載置面401に載置された第1構造体251を、載置面401押し付けることで、第1構造体251を載置面401に沿わせて湾曲させる。
次に、図42に示すように、第1構造体251の載置面401と反対側の空気袋81の表面に両面テープを貼り付けて接合層75を形成する。次に、この接合層75に、背板72を固定する。
次に、第2の固定を行う(ステップST32)。第2の固定では、背板72に、第2構造体252を固定する。具体例として、背板72の表面に両面テープを貼り付けて接合層75を形成する。次に、図43に示すように、第2構造体252を位置決め用の位置決めピン402にセットする。具体例として、第2構造体252の一方のピン用孔73aに、一方の位置決めピン402を配置し、他方のピン用孔73aに、他方の位置決めピン402を配置する。ここで言う一方のピン用孔73aは、シート96A、96Bのそれぞれの2つのピン用孔73aのうち、対向配置される一方のピン用孔73aである。他方のピン用孔73aは、対向配置される他方のピン用孔71aである。
次に、第2構造体252を背板72に押し付けることで、第2構造体252を背板72に固定する。
次に、第1構造体251の接合代94を、第2構造体252に接合する(ステップST33)。具体例として、接合代94の外縁部のうち、空気袋91の長手方向に沿う2つの縁部、及び第2構造体252の背板72側の空気袋81の溶着部81aの長手方向に沿う2つの縁部を高周波溶着機によって溶着することで、接合部94aを形成する。
このように、第1構造体251が接合代94によって第2構造体252に接合されることで、第1構造体251及び第2構造体252が一体化される。
次に、一体化された、第1構造体251、背板72、及び第2構造体252を裁断することで、押圧カフ71の形状、及びセンシングカフ73の形状に形成する(ステップST34)。裁断は、例えば、プレス機や、鋏によってなされる。
これらの工程により、カフユニット250が製造される。次に、製造したカフユニット250の所定の箇所に、ロット番号等の情報を印字する(ステップST35)。このように構成されるカフユニット250は、カーラ5の、押圧カフ71が固定される面に対応する曲面に構成された載置面401上で、第1構造体251及び第2構造体252が溶着されることで、カーラ5の、押圧カフ71が固定される内周面にならって湾曲する形状に構成される。
次に、図44に示すように、引張カフ74の製造方法の一例を説明する。
先ず、材料を裁断し(ステップST41)、所定の形状のシート部材106を形成する。なお、ここで、所定の形状とは、空気袋101及び被接合部102の形状に加え、溶着代や各加工機に位置合わせを行う位置合わせ用のダミー部等を含む形状である。具体例として、プレス機によって、熱可塑性樹脂材料で形成されたシート状の材料から、第7シート部材106a、第8シート部材106b、第9シート部材106c、第10シート部材106d、第11シート部材106e、第12シート部材106f、第13シート部材106g、第14シート部材106h、第15シート部材106i、第16シート部材106j、第17シート部材106k、及び第18シート部材106lをそれぞれ打ち抜く。
次に、第18シート部材106lに接続部103を溶着する(ステップST42)。具体例として、第18シート部材106lの中央側に設けられた孔部106l1に接続部103を差し込み、高周波溶着機によって、接続部103を第18シート106lに溶着する。
次に、ブリッジ溶着を行う(ステップST43)。具体例として、先ず、冶具の位置決めピンに第8シート部材106b及び第9シート部材106cを順次セットし、第8シート部材106b上に第9シート部材106cを重ねて配置する。次に、シート部材106b,106cの開口106b1,106c1を囲うように、高周波溶着機によって矩形枠状に溶着することで、ブリッジ溶着部101bを形成し、シート部材106b、106cを一体に溶着する。
次に、冶具の位置決めピンに第12シート部材106f及び第13シート部材106gを順次セットし、第12シート部材106f上に第13シート部材106gを重ねて配置する。次に、シート部材106g,106fの開口106g1,106f1を囲うように、高周波溶着機によって矩形枠状に溶着することで、ブリッジ溶着部101bを形成し、シート部材106g、106fを一体に溶着する。
次に、冶具の位置決めピンに第16シート部材106j及び第17シート部材106kを順次セットし、第16シート部材106j上に第17シート部材106kを重ねて配置する。次に、シート部材106j,106kの開口106j1,106k1を囲うように、高周波溶着機によって矩形枠状に溶着することで、ブリッジ溶着部101bを形成し、シート部材106j、106kを一体に溶着する。
次に、第1外層111を形成する(ステップST44)。具体的には、冶具の位置決めピンに、ステップST43でブリッジ溶着した第8シート部材106b及び第9シート部材106c、並びに第7シート部材106aを順次セットし、高周波溶着機によって、空気袋101の外周縁形状に溶着して、溶着部101aを形成する。これにより、第1外層111が形成される。
次に、第2外層114を形成する(ステップST45)。具体的には、冶具の位置決めピンに、ステップST33でブリッジ溶着した第16シート部材106j及び第17シート部材106k、並びに、ステップST42で接続部103を溶着した第18シート部材106lを順次セットし、高周波溶着機によって、空気袋101の外周縁形状に溶着して、溶着部101aを形成する。これにより、第2外層114が形成される。
次に、形成した第2外層114に被接合部102を形成する(ステップST46)。具体的には、冶具の位置決めピンに第2外層114をセットし、第6層の空気袋101、被接合部102及び切欠部104の外周縁形状に裁断可能な形状のプレス型にステップST45で形成した第2外層114を配置する。次に、第2外層114の上面に当て板を配置し、プレス加工機によりプレス加工することで、第2外層114は、第六層の空気袋101、被接合部102及び切欠部104の外周縁形状に裁断され、第2外層114に被接合部102が形成される。
次に、第1中間層112及び第2中間層113を形成する(ステップST47)。先ず、冶具の位置決めピンに、ステップST43でブリッジ溶着された第12シート部材106f及び第13シート部材106g間に中間電極を配置する。次に、第2外層114、ブリッジ溶着していないシート部材106h、106i、中間電極を間に配置したシート部材106g、106f、ブリッジ溶着していないシート部材106d、106e、及び、第1外層111を順次積層し、高周波溶着機によって、それぞれ空気袋101の外周縁形状に溶着して、溶着部101aを形成する。これにより、第1中間層112及び第2中間層113が形成される。即ち、第1外層111、第1中間層112、第2中間層113及び第2外層114の6層の空気袋101が形成される。
次に、形成した第1外層111、第1中間層112及び第2中間層113の仕上げ裁断する(ステップST48)。これらの工程により、引張カフ74が製造される。次に、製造した引張カフ74の所定の箇所に、ロット番号等の情報を印字する(ステップST49)。
次に、図45に示すように、血圧測定装置1の製造方法の一例を説明する。
先ず、カーラ5に給電部8を形成する(ステップST51)。カーラ5に配線部8a及び給電端子8bを構成するFPCをカーラ5のカバー部5a及び窪み5cに両面テープ等により接合し、窪み5cにカバー8cを両面テープ等により接合する。
次に、カーラ5にカフ構造体6を接合する(ステップST52)。具体例として、先ず、カフユニット250の押圧カフ71の第4シート部材86dのカーラ5と対向する領域、及び、被接合部82に接合層75である両面テープを貼り付けて、カーラ5に押圧カフ71を貼り付ける。押圧カフ71がカーラ5に接合層75により固定されることで、背板72及びセンシングカフ73も、同時にカーラ5に取り付けられる。なお、この工程において、押圧カフ71の接続部84及びセンシングカフ73の接続部93は、カーラ5のカバー部5aの第1孔部5f1及び第2孔部5f2に挿通させておく。
次に、引張カフ74の第18シート部材106lのカーラ5と対向する領域、及び、被接合部102に両面テープを貼り付けて、カーラ5並びにカーラ5の内面に配置された押圧カフ71の流路体83及びセンシングカフ73の流路体92に引張カフ74を貼り付ける。これらの工程により、カーラ5にカフ構造体6が接合される。
次に、カバー部5aにシール部材36及び裏カバー35を配置し、第1締結部材35aによりカバー部5aに裏カバー35を固定し(ステップST53)、裏蓋を構成する。
次に、裏カバー35を除く装置本体3を一体に組み立てる(ステップST54)。次に、装置本体3の外郭ケース31の手首200側の端部に裏カバー35を配置し、第2締結部材35bにより外郭ケース31及び裏カバー35を固定する(ステップST55)。そして、外郭ケース31に第1ベルト61及び第2ベルト62を組み立てる(ステップST56)。これらの工程により、血圧測定装置1が製造される。
次に、血圧測定装置1を使用した血圧値の測定の一例について、図46乃至図50を用いて説明する。図46は、血圧測定装置1を用いた血圧測定の一例を示す流れ図であり、ユーザの動作及び制御部55の動作の双方を示す。また、図47乃至図49は、ユーザが手首200に血圧測定装置1を装着する一例を示す。
先ず、ユーザは、手首200に血圧測定装置1を装着する(ステップST61)。具体例として、例えば、ユーザは、図47に示すように、手首200の一方をカーラ5内に挿入する。
このとき、血圧測定装置1は、装置本体3及びセンシングカフ73がカーラ5の相対する位置に配置されることから、センシングカフ73が手首200の手の平側の動脈210が存する領域に配置される。これにより、装置本体3及び引張カフ74は、手首200の手の甲側に配される。
次いで図48に示すように、ユーザが血圧測定装置1を配した手とは反対の手によって、第1ベルト61の尾錠61bの枠状体61eに第2ベルト62を通す。次いで、ユーザは、第2ベルト62を引っ張り、カーラ5の内周面側の部材、即ち、カフ構造体6を手首200に密着させ、小孔62aにつく棒61fを挿入する。これにより、図4及び図49に示すように、第1ベルト61及び第2ベルト62が接続され、血圧測定装置1が手首200に装着される。
次に、ユーザは、操作部13を操作して、血圧値の測定開始に対応した指令の入力を行う。指令の入力操作が行われた操作部13は、測定開始に対応した電気信号を制御部55へ出力する(ステップST62)。制御部55は、当該電気信号を受信すると、例えば、第1開閉弁16A、第2開閉弁16B及び第3開閉弁16Cを開くとともに、第4開閉弁16Dを閉じ、ポンプ14を駆動し、第1流路7a、第2流路7b、第3流路7c及び第4流路7dを介して押圧カフ71、センシングカフ73及び引張カフ74へ圧縮空気を供給する(ステップST63)。これにより、押圧カフ71、センシングカフ73及び引張カフ74は膨張を開始する。
第1圧力センサ17A及び第2圧力センサ17Bは、押圧カフ71、センシングカフ73及び引張カフ74の圧力を検出し、この圧力に対応した電気信号を制御部55へ出力する(ステップST64)。制御部55は、受信した電気信号に基づいて、押圧カフ71、センシングカフ73及び引張カフ74の内部空間の圧力が血圧測定のための所定の圧力に達しているか否かを判断する(ステップST65)。例えば、押圧カフ71及び引張カフ74の内圧が所定の圧力に達しておらず、且つ、センシングカフ73の内圧が所定の圧力に達した場合には、制御部55は、第1開閉弁16Aを閉じ、第2流路7b、第3流路7c、第4流路7dを介して圧縮空気を供給する。
押圧カフ71及び引張カフ74の内圧並びにセンシングカフ73の内圧が、全て所定の圧力に達した場合には、制御部55は、ポンプ14の駆動を停止する(ステップST65でYES)。このとき、図4に二点鎖線で示すように、押圧カフ71及び引張カフ74は十分に膨張しており、膨張した押圧カフ71は、背板72を押圧する。また、引張カフ74は、手首200から離間する方向に、カーラ5を押圧することから、ベルト4、カーラ5及び装置本体3は、手首200から離間する方向に移動し、結果、押圧カフ71、背板72、センシングカフ73が手首200側に引っ張られる。加えて、引張カフ74の膨張によってベルト4、カーラ5及び装置本体3が手首200から離間する方向に移動するときに、ベルト4及びカーラ5が、手首200の両側方に向かって移動し、手首200の両側方に密着した状態で、ベルト4、カーラ5及び装置本体3が移動する。このため、手首200の皮膚に密着したベルト4及びカーラ5は、手首200の両側方の皮膚を手の甲側に引っ張る。なお、カーラ5は、手首200の皮膚を引っ張ることができれば、例えば、シート部材86、106を介して間接的に手首200の皮膚に接触する構成であってもよい。
さらに、センシングカフ73は、内圧が血圧を測定するために要する圧力となるように所定の空気量が供給され、膨張しており、そして、押圧カフ71に押圧された背板72によって手首200に向かって押圧される。このため、センシングカフ73は、手首200内の動脈210を押圧し、図50に示すように動脈210を閉塞する。
また、制御部55は、例えば、第3開閉弁16Cを制御し、第3開閉弁16Cの開閉を繰り返すか、又は、第3開閉弁16Cの開度を調整することで、押圧カフ71の内部空間の圧力を加圧させる。この加圧の過程において第2圧力センサ17Bが出力する電気信号に基づいて、制御部55は、最高血圧及び最低血圧等の血圧値や心拍数等の測定結果を求める(ステップST66)。制御部55は、求めた測定結果に対応した画像信号を、表示部12へ出力し、測定結果を表示部12に表示する(ステップST67)。また、制御部55は、血圧測定終了後、第1開閉弁16A、第2開閉弁16B、第3開閉弁16C及び第4開閉弁16Dを開く。
表示部12は、画像信号を受信すると、当該測定結果を画面に表示する。使用者は、表示部12を視認することで、当該測定結果を確認する。なお、使用者は、測定終了後、小孔62aからつく棒61fを外し、枠状体61eから第2ベルト62を外し、カーラ5から手首200を抜くことで、手首200から血圧測定装置1を取り外す。
このように構成された本実施形態に係る血圧測定装置1は、センシングカフ73の接合代94が接合部94aにより押圧カフ71の空気袋81の溶着部81a、換言すると空気袋81の外縁部に接合されることで、押圧カフ71及びセンシングカフ73が固定されて一体化されることで、カフユニット250を構成する。
このように、押圧カフ71及びセンシングカフ73が固定されることで一体化したカフユニット250を構成することで、押圧カフ71及びセンシングカフ73を、一体物として、カーラ5に固定することが可能となる。
この為、カーラ5に対する一度の取り付け作業で、押圧カフ71及びセンシングカフ73を固定できるので、押圧カフ71及びセンシングカフ73を別々にカーラ5に対して固定する構成に比較して、カーラ5に対する押圧カフ71及びセンシングカフ73の位置ずれを抑制できる。
カーラ5に対する押圧カフ71及びセンシングカフ73の位置ずれを抑制できるので、カーラ5に対するセンシングカフ73の位置が大きくずれることが生じることを抑制できる。結果、血圧測定装置1の測定精度の低下を抑制できる。
さらに、カフユニット250を構成することで、押圧カフ71、背板72、及びセンシングカフ73をそれぞれカーラ5に対して固定する作業が不要になることで、血圧測定装置1を製造する作業の効率を向上できる。
さらに、接合代94がセンシングカフ73に一体に形成されることで、カフユニット250の部品数が増えることを抑制できる。
さらに、接合代94が、押圧カフ71の複数の空気袋81のうちセンシングカフ73の空気袋91に隣接する空気袋81に接合されることで、押圧カフ71の膨張が接合代94により阻害されることがない。
さらに、接合代94がセンシングカフ73の空気袋91の長手方向に沿う外縁部に形成され、かつ、接合代94の接合部94aが、押圧カフ71の背板72側の空気袋81の長手方向に沿う外縁部となる溶着部81aに接合されることで、接合部94aが、空気袋81の溶着部81aの広い範囲、及び、カーラ5の外側に面する範囲に接合される。結果、押圧カフ71及びセンシングカフ73の間に、ユーザの汗等の水が浸入することを抑制できる。
さらに、カフユニット250は、冶具400により製造されることで、冶具400から取り外されてカーラ5に固定される前の状態において、カーラ5の押圧カフ71が接合される面に倣って湾曲する形状に構成される。この為、カフユニット250をカーラ5に接合したときに、押圧カフ71及びセンシングカフ73に、膨張を阻害するしわが発生することを抑制できる。
さらに、カフユニット250が背板72を備える構成であることから、押圧カフ71、背板72、及びセンシングカフ73の一体物をカーラ5に一度の取り付け作業で固定できるので、血圧測定装置1の製造工程数を低減できる。
さらに、カーラ5の、押圧カフ71が固定される面に対応する曲面に構成された載置面401を有する冶具400を用いて、押圧カフ71及びセンシングカフ73を一体に固定することで、押圧カフ71及びセンシングカフ73を、湾曲した姿勢で、一体に固定できる。結果、押圧カフ71及びセンシングカフ73が一体に固定されたカフユニット250をカーラ5に固定したときに、押圧カフ71の空気袋81、及びセンシングカフ73の空気袋91にしわが生じて空気袋81、91の膨張が阻害されるという状態が生じることを抑制できる。すなわち、押圧カフ71及びセンシングカフ73を、平面状の載置面を有する冶具を用いて一体に固定してカフユニットを構成すると、カフユニットは、平面状の載置面に合わせて、センシングカフ73の上面が平面となる形状に構成される。このカフユニットをカーラ5に固定すると、カフユニットがカーラ5の形状に合わせて湾曲することで生じる内外周差によって、空気袋81、91にしわが生じる可能性がある。
しかしながら、本実施形態では、載置面401を有する冶具400を用いて、押圧カフ71及びセンシングカフ73を接合代94による接合による固定により一体化することで、カフユニット250をカーラ5に固定したときに、空気袋81、91に、膨張を阻害するしわが発生することを抑制できる。
さらに、冶具400が位置決め用のピン402を複数有し、第1構造体251が複数のピン用孔71aを有し、かつ、第2構造体252が複数のピン用孔73aを有する。そして、第1構造体251及び第2構造体252は、それぞれがピン402にセットして位置決めされた状態で、固定して一体化される。この為、押圧カフ71に対するセンシングカフ73の位置ずれの発生を抑制できる。
さらに、ピン用孔71aは、第1構造体251を製造する工程で、金型302のピン301による金型302への位置決めにも用いられる。この為、ピン用孔71aに対する押圧カフ71の位置が固定される。さらに、ピン用孔73aは、第2構造体252を製造する工程で、金型320のピン321による金型320への位置決めに用いられる。この為、ピン用孔73aに対するセンシングカフ73の位置が固定される。このように、ピン用孔71a、73aが、構造体251、252の製造工程、及びカフユニット250の製造工程で用いられることで、押圧カフ71に対するセンシングカフ73の位置ずれの発生を、より一層抑制できる。
さらに、位置決めピン402が複数設けられ、ピン用孔71a、73aがそれぞれ複数設けられ、複数の位置決めピン402が複数のピン用孔71a、73aにセットされることで、載置面401に対して、構造体251、252が位置決めピン402回りに回転する等の移動することを抑制できる。
さらに、第1構造体251及び第2構造体252を固定して一体化した後に裁断を行うことで、カフユニット250の製造の作業効率を向上できる。
なお、本実施形態の血圧測定装置1は、センシングカフ73の接合代94が、接合部94aによって、押圧カフ71の背板72側の空気袋81の長手方向に沿う2つの縁部に設けられる溶着部81aに接合される構成が一例として説明されたが、これに限定されない。センシングカフ73は、例えば、空気袋81を囲む環状に構成される接合部94aにより、押圧カフ71に固定されてもよい。この構成では、接合代94は、空気袋91の溶着部91a及び流路体92の溶着部92aに連続して形成される。そして、接合代94の長手方向に沿う外縁部が、空気袋81の長手方向に沿う溶着部81aに接合される。そして、接合代94の短手方向に沿う外縁部が空気袋81の短手方向に沿う溶着部81aに接合される。そして、流路体92の一部が、押圧カフ71の背板72側の空気袋81の溶着部81aの一部に固定される。流路体92及び溶着部81aの固定は、溶着以外の固定手段により固定されてもよい。この固定手段は、例えば、両面テープや接着剤である。
また、本実施形態では、第1構造体251及び第2構造体252がそれぞれ別々に製造され、第2構造体252の接合代94を第1構造体251に接合する製造方法が一例として説明されたが、これに限定されない。他の例では、第1構造体251の製造工程において、ステップST14及び図29に示すように、押圧カフ71のセンシングカフ73側の空気袋81を構成する第1シート86A及び第2シート86Bを溶着して溶着部81aを形成する工程で、第2構造体252の接合代94も同時に溶着して接合してもよい。換言すると、一度の溶接により、溶着部81a及び接合部94aを形成してもよい。
この一例として、図51に示すように、金型302に、溶着された第2シート86B及び第3シート86Cを配置し、第2シート86B上に第1シート86Aを配置し、さらに、第1シート86A上に、第2構造体252を配置する。このとき、それぞれのピン用孔71a,73aは、金型302のピン301に配置されて位置決めされる。
そして、第2構造体252の接合代94を構成する第5シート96A及び第6シート96Bと、第1シート86A及び第2シート86Bと、を溶着することで、溶着部81a及び接合部94aとを同時に形成する。なお、図51では、第2構造体252は、接合部94aの近傍のみを示しており、他の構成は省略している。
また、本実施形態の血圧測定装置1は、接合代94が、センシングカフ73を構成する2枚のシート部材96a、96bにより構成される例が一例として説明されたが、これに限定されない。接合代94は、例えば図52及び図53に示すように、シート部材96aまたはシート部材96bに形成されてもよい。
図53に示すように、接合代94が、手首200側に配置される第5シート部材96aに形成されることで、センシングカフ73の手首200側の表面に、シート部材96aの厚みによる段差が形成されることが抑制される。この為、この段差に起因して手首200及びセンシングカフ73の間に隙間が形成されることを抑制できるので、血圧測定装置1の測定精度が低下することを抑制できる。
なお、図52及び図53に示すように、接合代94が、第5シート部材96aまたは第6シート部材96bに形成される構成であっても、図51に示すように、接合代94と、空気袋81を構成する第1シート86A及び第2シート86Bと、を同時に溶着することで、溶着部81a及び接合部94aを同時に形成してもよい。この場合では、3枚のシートが同時に溶着される。
また、本実施形態の血圧測定装置1は、第1構造体251及び第2構造体252を接合代94の接合部94aにより接合することで一体にした後に、裁断を施すことで、押圧カフ71の形状に形成し、かつセンシングカフ73の形状に形成する製造方法により製造される一例が説明されたが、これに限定されない。
他の例では、第1構造体251を形成した後、第1構造体251に裁断を施すことで、押圧カフ71に近い形状に形成し、第2構造体252を形成した後、第2構造体252に裁断を施すことで、センシングカフ73に近い形状に形成し、これらを、冶具400を用いて、接合部94aにより接合することで一体に固定してもよい。なお、ここで言う押圧カフ71に近い形状とは、押圧カフ71の外形にピン用孔71aを構成する程度の裁断代を残す形状である。センシングカフ73に近い形状とは、センシングカフ73の外形にピン用孔73aを構成する程度の裁断代を残す形状である。そして、押圧カフ71及びセンシングカフ73を一体化した後、ピン用孔71aを構成する裁断代、及びピン用孔73aを構成する裁断代を裁断する。
また、本実施形態の血圧測定装置1では、第1構造体251のシート部材の溶着工程(ステップST14)は、図29乃至図31に示すように、ブリッジ溶着されて一体化した第2シート86B及び第3シート86Cの第2シート86Bに第1シート86Aを溶着して一体化し、溶着されて一体化した第1シート86A、第2シート86B、及び第3シート86Cに第4シート86Dを溶着する工程を一例として説明されたがこれに限定されない。第1構造体251のシート部材の溶着工程(ステップST14)は、例えば、ブリッジ溶着されて一体化した第2シート86B及び第3シート86Cの第2シート86Bと、第1シート86Aの溶着と、ブリッジ溶着されて一体化した第2シート86B及び第3シート86Cの第3シート86Cと、第4シート86Dの溶着と、を一度の工程で行ってもよい。この一例として、以下の方法がある。
先ず、ブリッジ溶着した第2シート86B及び第3シート86Cの間に中間電極を配置する。次に、冶具の位置決めピンに第1シート86A、中間電極を配置した第2シート86B及び第3シート86C、並びに、接続部84が溶着された第4シート86Dを順次セットし、シート86A、86B、86C、86Dを重ねて配置する。そして、シート86A、86B、86C、86Dを高周波溶着機によって押圧カフ71の外周形状に溶着し、溶着部81a、83aを形成し、シート86A、86B、86C、86Dを一体に溶着する。これにより、空気袋81及び流路体83が形成される。
また、本実施形態の血圧測定装置1では、接合代94は、押圧カフ71の空気袋81の外縁部に接合される構成として、溶着部81aに接合される構成が一例として説明されたが、これに限定されない。接合代94は、空気袋81の外面において、外縁よりも内側であって当該外縁の周囲の領域に固定されてもよい。ここで言う、空気袋81の外面において外縁より内側であって当該外縁の周囲の領域は、空気袋81の外縁部の一例である。
なお、本発明は上述した実施形態に限定されない。上述した実施形態では、センシングカフ73の接合代94を押圧カフ71に接合する接合手段として熱による溶着が用いられる構成が一例として説明されたが、これに限定されない。他の例では、熱以外の溶着が用いられてもよい。また、接合手段は、他の例では、接着剤や、両面テープであってもよい。
また、本実施形態では、第1構造体251の上に背板72を配置して接合層75により固定した後、第1構造体251及び背板72上に、第2構造体252を配置して第2構造体及び背板72を接合層75により固定し、その後で、第1構造体251及び第2構造体252を溶着により一体に固定する製造方法が一例として説明されたが、これに限定されない。
例えば、第1構造体251上に第2構造体252を配置して第1構造体251及び第2構造体252を溶着により固定して一体化した後に、第1構造体251及び第2構造体252間に背板72を配置して背板72を第1構造体251及び第2構造体252に固定してもよい。
また、本実施形態では、冶具400の載置面401に、第1構造体251、背板72、及び第2構造体252が順次配置される製造方法が一例として説明されたが、これに限定されない。他の例では、第1構造体251及び背板72を一体に固定した後、これら一体物を冶具400の位置決めピン402にセットし、次に第2構造体252を位置決めピン402にセットし、次に、背板72及び第2構造体252を固定し、次に第1構造体251及び第2構造体252を溶着により固定して一体化してもよい。
また、本実施形態では、第1構造体251及び第2構造体252は、それぞれ、平板状に形成された後、冶具400の載置面401に載置されることで、載置面401に沿って湾曲される例が一例として説明されたが、これに限定されない。第1構造体251及び第2構造体252は、それぞれ、カーラ5の押圧カフ71が配置される面に対応した曲面に構成された載置面を有する金型により形成されることで、カーラ5の押圧カフ71が配置される面に対応した曲面に沿って湾曲した状態で、溶着部81a、83a、91a、92aが形成されてもよい。
また、本実施形態では、背板72は、一例として、両面テープにより構成される接合層75により、押圧カフ71及びセンシングカフ73に固定される構成が一例として説明されたが、これに限定されない。背板72は、接着剤等の、両面テープ以外の固定手段により固定されてもよい。
また、本実施形態では、冶具400の載置面401は、少なくとも空気袋81の全域及び空気袋91を配置可能な構成として、空気袋81の全域、空気袋91の全域、流路体83の一部、及び流路体92の一部を配置可能な大きさを有する構成が一例として説明されたが、これに限定されない。載置面401は、空気袋81の全域、流路体83の全域、空気袋91の全域、及び流路体92の全域を配置可能な大きさを有してもよい。
また、本実施形態では、押圧カフ71は、複数の空気袋81を備える構成として、2つの空気袋81を備える構成が一例として説明されたが、これに限定されない。押圧カフ71は、例えば3つ以上の空気袋81を備える構成であってもよい。
即ち、本発明は、上記実施形態に限定されるものではなく、実施段階ではその要旨を逸脱しない範囲で種々に変形することが可能である。また、各実施形態は可能な限り適宜組み合わせて実施してもよく、その場合組み合わせた効果が得られる。更に、上記実施形態には種々の段階の発明が含まれており、開示される複数の構成要件における適当な組み合わせにより種々の発明が抽出され得る。
1…血圧測定装置
3…装置本体
4…ベルト
5…カーラ
5a…カバー部
5b…逃げ部
5c…窪み
5d…インサート部材
5e…螺子孔
5f…孔部
5f1…第1孔部
5f2…第2孔部
5f3…第3孔部
6…カフ構造体
7…流体回路
7a…第1流路
7b…第2流路
7c…第3流路
7d…第4流路
8…給電部
8a…配線部
8b…給電端子
8c…カバー
11…ケース
12…表示部
13…操作部
14…ポンプ
15…流路部
16…開閉弁
16A…第1開閉弁
16B…第2開閉弁
16C…第3開閉弁
16D…第4開閉弁
17…圧力センサ
17A…第1圧力センサ
17B…第2圧力センサ
18…電力供給部
19…振動モータ
20…制御基板
31…外郭ケース
31a…ラグ
31b…バネ棒
32…風防
33…基部
35…裏カバー
35a…第1締結部材
35b…第2締結部材
35c…孔部
35d…孔部
36…シール部材
41…釦
42…センサ
43…タッチパネル
51…基板
52…加速度センサ
53…通信部
54…記憶部
55…制御部
56…メインCPU
57…サブCPU
61…第1ベルト
61a…ベルト部
61b…尾錠
61c…第1孔部
61d…第2孔部
61e…枠状体
61f…つく棒
62…第2ベルト
62a…小孔
62b…第3孔部
71…押圧カフ
71a…ピン用孔
72…背板
72a…溝
73…センシングカフ
73a…ピン用孔
74…引張カフ
75…接合層
81…空気袋(第1袋状構造体)
81a…溶着部
81b…ブリッジ溶着部
82…被接合部
83…流路体
83a…溶着部
84…接続部
86…シート部材
86a…第1シート部材
86b…第2シート部材
86b1…開口
86c…第3シート部材
86c1…開口
86d…第4シート部材
86d1…孔部
91…空気袋(第2袋状構造体)
91a…溶着部
92…流路体
92a…溶着部
93…接続部
94…接合代
94a…接合部
96…シート部材
96a…第5シート部材
96b…第6シート部材
96b1…孔部
101…空気袋
101a…溶着部
101b…ブリッジ溶着部
102…被接合部
102a…逃げ部
103…接続部
104…切欠部
106…シート部材
106a…第7シート部材
106b…第8シート部材
106b1…開口
106c…第9シート部材
106c1…開口
106d…第10シート部材
106d1…開口
106e…第11シート部材
106e1…開口
106f…第12シート部材
106f1…開口
106g…第13シート部材
106g1…開口
106h…第14シート部材
106h1…開口
106i…第15シート部材
106i1…開口
106j…第16シート部材
106j1…開口
106k…第17シート部材
106k…シート部材
106k1…開口
106l…第18シート部材
106l1…孔部
111…第1外層
112…第1中間層
113…第2中間層
114…第2外層
200…手首
250…カフユニット
251…第1構造体
252…第2構造体
210…動脈
301…位置決めピン
302…下金型
302a…電極部
302b…空洞
320…下金型
321…位置決めピン
322…電極部
400…冶具
401…載置面
402…位置決めピン
3…装置本体
4…ベルト
5…カーラ
5a…カバー部
5b…逃げ部
5c…窪み
5d…インサート部材
5e…螺子孔
5f…孔部
5f1…第1孔部
5f2…第2孔部
5f3…第3孔部
6…カフ構造体
7…流体回路
7a…第1流路
7b…第2流路
7c…第3流路
7d…第4流路
8…給電部
8a…配線部
8b…給電端子
8c…カバー
11…ケース
12…表示部
13…操作部
14…ポンプ
15…流路部
16…開閉弁
16A…第1開閉弁
16B…第2開閉弁
16C…第3開閉弁
16D…第4開閉弁
17…圧力センサ
17A…第1圧力センサ
17B…第2圧力センサ
18…電力供給部
19…振動モータ
20…制御基板
31…外郭ケース
31a…ラグ
31b…バネ棒
32…風防
33…基部
35…裏カバー
35a…第1締結部材
35b…第2締結部材
35c…孔部
35d…孔部
36…シール部材
41…釦
42…センサ
43…タッチパネル
51…基板
52…加速度センサ
53…通信部
54…記憶部
55…制御部
56…メインCPU
57…サブCPU
61…第1ベルト
61a…ベルト部
61b…尾錠
61c…第1孔部
61d…第2孔部
61e…枠状体
61f…つく棒
62…第2ベルト
62a…小孔
62b…第3孔部
71…押圧カフ
71a…ピン用孔
72…背板
72a…溝
73…センシングカフ
73a…ピン用孔
74…引張カフ
75…接合層
81…空気袋(第1袋状構造体)
81a…溶着部
81b…ブリッジ溶着部
82…被接合部
83…流路体
83a…溶着部
84…接続部
86…シート部材
86a…第1シート部材
86b…第2シート部材
86b1…開口
86c…第3シート部材
86c1…開口
86d…第4シート部材
86d1…孔部
91…空気袋(第2袋状構造体)
91a…溶着部
92…流路体
92a…溶着部
93…接続部
94…接合代
94a…接合部
96…シート部材
96a…第5シート部材
96b…第6シート部材
96b1…孔部
101…空気袋
101a…溶着部
101b…ブリッジ溶着部
102…被接合部
102a…逃げ部
103…接続部
104…切欠部
106…シート部材
106a…第7シート部材
106b…第8シート部材
106b1…開口
106c…第9シート部材
106c1…開口
106d…第10シート部材
106d1…開口
106e…第11シート部材
106e1…開口
106f…第12シート部材
106f1…開口
106g…第13シート部材
106g1…開口
106h…第14シート部材
106h1…開口
106i…第15シート部材
106i1…開口
106j…第16シート部材
106j1…開口
106k…第17シート部材
106k…シート部材
106k1…開口
106l…第18シート部材
106l1…孔部
111…第1外層
112…第1中間層
113…第2中間層
114…第2外層
200…手首
250…カフユニット
251…第1構造体
252…第2構造体
210…動脈
301…位置決めピン
302…下金型
302a…電極部
302b…空洞
320…下金型
321…位置決めピン
322…電極部
400…冶具
401…載置面
402…位置決めピン
Claims (10)
- 積層され、それぞれが流体により膨張する複数の第1袋状構造体を含み、カーラに接合される押圧カフと、
流体により膨張する1つの第2袋状構造体、及び前記第2袋状構造体に形成され、前記第2袋状構造体に隣接する前記第1袋状構造体に接合される接合代を含むセンシングカフと、
を備えるカフユニット。 - 前記第1袋状構造体は、一方向に長い形状に構成され、
前記第2袋状構造体は、一方向に長い形状に構成され、
前記接合代は、前記第2袋状構造体の長手方向に沿う外縁部に形成され、前記第1袋状構造体の長手方向に沿う外縁部に接合される
請求項1に記載のカフユニット。 - 前記押圧カフ及び前記センシングカフは、前記カーラの内周面にならって湾曲する
請求項1に記載のカフユニット。 - 前記押圧カフ及び前記センシングカフの間に配置され、前記押圧カフ及び前記センシングカフに接合される背板を備える、請求項1に記載のカフユニット。
- カーラの押圧カフが接合される面に対応する曲面に形成された載置面を有する冶具の前記載置面に、前記押圧カフを含む第1構造体を配置して前記載置面に対する前記第1構造体の位置決めをし、
前記第1構造体上に、センシングカフを含む第2構造体を配置して前記載置面に対する前記第2構造体の位置決めをし、
前記第1構造体及び前記第2構造体を接合して一体化する
カフユニットの製造方法。 - 前記第2構造体は、接合代を含み、
前記第1構造体及び前記第2構造体は、前記接合代で接合される
請求項5に記載のカフユニットの製造方法。 - 前記第1構造体上に背板を配置して前記背板を前記第1構造体に接合した後、前記第1構造体及び前記背板上に前記第2構造体を配置して、前記第2構造体を前記第1構造体及び前記背板に接合する
請求項5に記載のカフユニットの製造方法。 - 前記冶具は、複数の位置決めピンを有し、
前記第1構造体は、前記位置決めピンを配置する孔を複数有し、
前記第2構造体は、前記位置決めピンを配置する孔を複数有し、
前記複数の位置決めピンが、前記第1構造体の複数の前記孔、及び前記第2構造体の複数の前記孔にセットされた状態で、前記接合代が前記第1構造体に接合される
請求項6に記載のカフユニットの製造方法。 - 前記第1構造体及び前記第2構造体は、それぞれ、裁断代を含み、
前記第1構造体、及び前記第2構造体を固定して一体化した後に、前記裁断代を裁断する
請求項5に記載のカフユニットの製造方法。 - カーラと、
積層され、それぞれが流体により膨張する複数の第1袋状構造体を含み、カーラに接合される押圧カフ、並びに、流体により膨張する1つの第2袋状構造体、及び前記第2袋状構造体に形成され、前記第2袋状構造体に隣接する前記第1袋状構造体に接合される接合代を含むセンシングカフを備えるカフユニットと、
前記カフユニットに前記流体を供給する装置本体と、
を備える血圧測定装置。
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE112020000608.5T DE112020000608T5 (de) | 2019-03-15 | 2020-02-17 | Manschetteneinheit, verfahren zur herstellung einer manschetteneinheit und blutdruckmessvorrichtung |
| CN202080013720.5A CN113423332B (zh) | 2019-03-15 | 2020-02-17 | 袖带单元、袖带单元的制造方法以及血压测定装置 |
| US17/447,351 US20220000379A1 (en) | 2019-03-15 | 2021-09-10 | Cuff unit, method for manufacturing cuff unit, and blood pressure measuring device |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2019048855A JP7278814B2 (ja) | 2019-03-15 | 2019-03-15 | カフユニット、カフユニットの製造方法、及び血圧測定装置 |
| JP2019-048855 | 2019-03-15 |
Related Child Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| US17/447,351 Continuation US20220000379A1 (en) | 2019-03-15 | 2021-09-10 | Cuff unit, method for manufacturing cuff unit, and blood pressure measuring device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2020189125A1 true WO2020189125A1 (ja) | 2020-09-24 |
Family
ID=72431408
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2020/005959 Ceased WO2020189125A1 (ja) | 2019-03-15 | 2020-02-17 | カフユニット、カフユニットの製造方法、及び血圧測定装置 |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US20220000379A1 (ja) |
| JP (1) | JP7278814B2 (ja) |
| CN (1) | CN113423332B (ja) |
| DE (1) | DE112020000608T5 (ja) |
| WO (1) | WO2020189125A1 (ja) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2024161725A1 (ja) * | 2023-02-01 | 2024-08-08 | オムロンヘルスケア株式会社 | 血圧測定装置 |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2023125276A (ja) * | 2022-02-28 | 2023-09-07 | ソニーグループ株式会社 | 触覚提示装置及び触覚提示層 |
| EP4260799A1 (en) * | 2022-04-15 | 2023-10-18 | Hinlab | Wearable blood pressure monitoring device |
| KR102944222B1 (ko) * | 2023-05-19 | 2026-03-30 | (주)참케어 | 혈압 측정 장치용 커프 및 이를 포함하는 혈압 측정 장치 |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2018123284A1 (ja) * | 2016-12-28 | 2018-07-05 | オムロン株式会社 | 脈波測定装置および脈波測定方法、並びに血圧測定装置 |
| WO2018146967A1 (ja) * | 2017-02-07 | 2018-08-16 | オムロン株式会社 | 袋状構造体、血圧計用カフ、及び血圧計 |
| WO2018179645A1 (ja) * | 2017-03-27 | 2018-10-04 | オムロン株式会社 | 血圧計、血圧測定装置及び血圧測定方法 |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH11309119A (ja) | 1998-04-27 | 1999-11-09 | Omron Corp | 血圧計用カフ |
| JP2004283320A (ja) * | 2003-03-20 | 2004-10-14 | Colin Medical Technology Corp | 二重カフ |
| JP4654641B2 (ja) * | 2004-09-15 | 2011-03-23 | オムロンヘルスケア株式会社 | 血圧計用カフ |
| JP4742576B2 (ja) * | 2004-12-10 | 2011-08-10 | オムロンヘルスケア株式会社 | 血圧計用カフおよびこれを備えた血圧計 |
| JP4595525B2 (ja) * | 2004-12-20 | 2010-12-08 | オムロンヘルスケア株式会社 | 血圧計用カフおよびこれを備えた血圧計 |
| JP2009213767A (ja) * | 2008-03-12 | 2009-09-24 | Omron Healthcare Co Ltd | 血圧情報測定装置 |
| JP5418302B2 (ja) * | 2010-02-26 | 2014-02-19 | オムロンヘルスケア株式会社 | 血圧情報測定装置 |
-
2019
- 2019-03-15 JP JP2019048855A patent/JP7278814B2/ja active Active
-
2020
- 2020-02-17 CN CN202080013720.5A patent/CN113423332B/zh active Active
- 2020-02-17 DE DE112020000608.5T patent/DE112020000608T5/de active Pending
- 2020-02-17 WO PCT/JP2020/005959 patent/WO2020189125A1/ja not_active Ceased
-
2021
- 2021-09-10 US US17/447,351 patent/US20220000379A1/en active Pending
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2018123284A1 (ja) * | 2016-12-28 | 2018-07-05 | オムロン株式会社 | 脈波測定装置および脈波測定方法、並びに血圧測定装置 |
| WO2018146967A1 (ja) * | 2017-02-07 | 2018-08-16 | オムロン株式会社 | 袋状構造体、血圧計用カフ、及び血圧計 |
| WO2018179645A1 (ja) * | 2017-03-27 | 2018-10-04 | オムロン株式会社 | 血圧計、血圧測定装置及び血圧測定方法 |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2024161725A1 (ja) * | 2023-02-01 | 2024-08-08 | オムロンヘルスケア株式会社 | 血圧測定装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2020146394A (ja) | 2020-09-17 |
| CN113423332B (zh) | 2024-10-18 |
| CN113423332A (zh) | 2021-09-21 |
| JP7278814B2 (ja) | 2023-05-22 |
| US20220000379A1 (en) | 2022-01-06 |
| DE112020000608T5 (de) | 2021-10-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP7094876B2 (ja) | 血圧測定装置用カフの製造方法 | |
| JP7150595B2 (ja) | 血圧測定装置用カフカバー | |
| JP7237576B2 (ja) | 血圧測定装置 | |
| JP7278814B2 (ja) | カフユニット、カフユニットの製造方法、及び血圧測定装置 | |
| WO2020137483A1 (ja) | 血圧測定装置 | |
| JP7202886B2 (ja) | 血圧測定装置 | |
| JP7094875B2 (ja) | 血圧測定装置 | |
| JP7175738B2 (ja) | 血圧測定装置 | |
| CN112689472B (zh) | 血压测定装置 | |
| JP7118852B2 (ja) | 血圧測定装置 | |
| JP7237574B2 (ja) | 血圧測定装置 | |
| JP7202885B2 (ja) | 血圧測定装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 20774194 Country of ref document: EP Kind code of ref document: A1 |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 20774194 Country of ref document: EP Kind code of ref document: A1 |