WO2020175397A1 - 建具、及び建具の製造方法 - Google Patents
建具、及び建具の製造方法 Download PDFInfo
- Publication number
- WO2020175397A1 WO2020175397A1 PCT/JP2020/007191 JP2020007191W WO2020175397A1 WO 2020175397 A1 WO2020175397 A1 WO 2020175397A1 JP 2020007191 W JP2020007191 W JP 2020007191W WO 2020175397 A1 WO2020175397 A1 WO 2020175397A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- plate
- resin layer
- core material
- door structure
- shaped body
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B5/00—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts
- B32B5/18—Layered products characterised by the non- homogeneity or physical structure, i.e. comprising a fibrous, filamentary, particulate or foam layer; Layered products characterised by having a layer differing constitutionally or physically in different parts characterised by features of a layer of foamed material
-
- E—FIXED CONSTRUCTIONS
- E06—DOORS, WINDOWS, SHUTTERS, OR ROLLER BLINDS IN GENERAL; LADDERS
- E06B—FIXED OR MOVABLE CLOSURES FOR OPENINGS IN BUILDINGS, VEHICLES, FENCES OR LIKE ENCLOSURES IN GENERAL, e.g. DOORS, WINDOWS, BLINDS, GATES
- E06B3/00—Window sashes, door leaves, or like elements for closing wall or like openings; Layout of fixed or moving closures, e.g. windows in wall or like openings; Features of rigidly-mounted outer frames relating to the mounting of wing frames
- E06B3/70—Door leaves
-
- E—FIXED CONSTRUCTIONS
- E06—DOORS, WINDOWS, SHUTTERS, OR ROLLER BLINDS IN GENERAL; LADDERS
- E06B—FIXED OR MOVABLE CLOSURES FOR OPENINGS IN BUILDINGS, VEHICLES, FENCES OR LIKE ENCLOSURES IN GENERAL, e.g. DOORS, WINDOWS, BLINDS, GATES
- E06B3/00—Window sashes, door leaves, or like elements for closing wall or like openings; Layout of fixed or moving closures, e.g. windows in wall or like openings; Features of rigidly-mounted outer frames relating to the mounting of wing frames
- E06B3/70—Door leaves
- E06B3/82—Flush doors, i.e. with completely flat surface
Definitions
- the present invention relates to a fitting and a method for manufacturing the fitting.
- Patent Document 1 discloses a door fitting with a mirror.
- Patent Document 1 Japanese Utility Model Publication No. 6-2-0 0 0 6 8 7
- the core material is made of metal or resin
- warping may occur due to a force from an unintended direction.
- the warp of the core material causes the warp of the fitting.
- the weight of fittings is required to be reduced in order to reduce the burden of transportation and construction.
- the present invention has been made in view of the above problems, and an object of the present invention is to provide a fitting that can alleviate warp of a core material and that can be reduced in weight, and a method for manufacturing the fitting.
- the fitting according to the first aspect includes a flat-plate-shaped core material having a first surface and a second surface facing each other, and a first resin layer that is a foam disposed on the first surface side of the core material.
- a fitting according to a second aspect includes a flat-plate-shaped core material having a first surface and a second surface facing each other, and a first resin layer that is a foam disposed on the first surface side of the core material.
- a second resin layer which is a foam body, arranged on the second surface side of the material, and a brittle second plate having a design property arranged on the surface opposite to the surface on which the core material of the second resin layer is arranged.
- a laminated body including a body.
- a method for manufacturing a fitting according to a third aspect is a flat plate-shaped core material having a first surface and a second surface facing each other, and a foam body arranged on the side of the first surface of the core material.
- a first resin layer, a first resin layer, a laminate containing a brittle first plate having a design disposed on the surface of the first resin layer opposite to the core material is prepared, the core material is cut, In addition, cutting the _ part on the core material side of the first resin layer is included.
- FIG. 1 is a schematic sectional view showing a part of a door structure according to a first embodiment of the present invention.
- FIG. 2 is a schematic sectional view showing a part of a door structure according to a second embodiment of the present invention.
- FIG. 3 is a perspective view of a door structure according to a third embodiment of the present invention.
- Fig. 4 is a schematic sectional view showing a part of the door structure shown in Fig. 3.
- FIG. 5 is a schematic cross-sectional view showing a part of a door structure according to another form of the third embodiment.
- FIG. 6 is an explanatory view showing one step of one embodiment of a method for manufacturing a door structure according to the present invention.
- FIG. 7 is an explanatory view showing one step of a method for manufacturing a door structure.
- FIG. 8 is an explanatory view showing one step of a method for manufacturing a door structure.
- FIG. 9 is an explanatory view showing one step of a method for manufacturing a door structure.
- Fig. 10 shows the warp amount 1 to 1. The test method for calculating is shown.
- Fig. 11 shows the test method for calculating the amount of warpage! I 1 .
- Figure 12 shows the amount of warp! ⁇ Indicates the test method for calculating I 1 .
- FIG. 1 is a schematic sectional view showing a door structure 10 according to the first embodiment.
- the door structure 10 includes a core material 12, a resin layer 14 and a laminated body 17 including a plate-like body 16.
- the core material 12 has a flat plate shape having a first surface 1 28 and a second surface 1 2 which face each other. It should be noted that it is possible to arbitrarily determine which of the two main surfaces of the core material 12 facing each other is the first surface 1 28 and the second surface 12 2.
- the first resin layer 14 is a resin layer that is a foam, and is arranged on the first surface 12 28 side of the core material 12.
- the plate-like body 16 is a brittle first plate-like body having a design property, and is arranged on the surface of the resin layer 14 opposite to the core material 12.
- the core material 12 and the plate-shaped body 16 are arranged at positions facing each other with the resin layer 14 in between.
- the design layer 18 is arranged between the plate-like body 16 and the resin layer 14.
- the designability of the plate-shaped body 16 is imparted by the design layer 18 interposed between the plate-shaped body and the resin layer.
- the design of the plate-shaped body 16 is the plate-shaped body itself. ⁇ 0 2020/175 397 4 (: 17 2020/007191
- the design layer 18 interposed between the plate-shaped body 16 and the resin layer 14 is formed directly on the surface of the plate-shaped body 16 and on the surface of the resin layer 14. Including the form of the designed layer
- the door structure 10 includes the design layer 18, the door structure 10 can produce a high-class aesthetic appearance when used as an entrance/exit of a building or an opening of a storage house.
- the overall thickness of the door structure 10 according to the first embodiment is more preferably 10 or more, and 15 The above is more preferable.
- the total thickness of the door structure 10 of the first embodiment is 2 The following is more preferable, 1 The following is more preferable, The following are particularly preferred.
- the entire first surface 1228 of the core material 12 is covered with the resin layer 14 and the plate-shaped body 16; A part of the first surface 12 8 of the material 12 may be covered with the resin layer 14 and the plate-shaped body 16.
- the ratio of the area covered by the resin layer 14 and the plate-shaped body 16 to the area of the first surface 12 of the core 12 is preferably 80% or more, more preferably 90% or more. , 95% or more is more preferable.
- the ratio of the area covered by the resin layer 14 and the plate-shaped body 16 to the area of the first surface 12 28 of the core material 12 may be 100% or less, 9 It may be 7% or less.
- the area of the door structure 1 0 of the first embodiment 0.0 1 2 or more, 0. 1 are more preferred, ⁇ . 5 2 or more, and particularly preferably 1 2 or more, 2. 5 2 or more is most preferable.
- the door structure 10 has a large area and tends to warp and becomes heavy, the presence of the resin layer 14 reduces the warp and makes it lighter.
- the area of the door structure 1 ⁇ of the first embodiment may it der 5 2 or less, may be four 2 or less, 3.5 may be two or less, even 3 Good.
- the first surface 1 2 eighth of the core member 1 2, the area of a portion covered by the resin layer 1 4 and the plate-like body 1 6 0.0 1 2 or more, ⁇ . 1 2 or more is better ⁇ 02020/175397 5 ⁇ (: 170? 2020 /007191
- Mashiku 0. 5 m 2 or more, and particularly preferably 1 m 2 or more, 2.
- the area of the portion of the first surface 12 A of the core 12 covered with the resin layer 14 and the plate-like body 16 may be 5 m 2 or less, or 4 m It may be 2 or less, 3.5 m 2 or less, or 3 m 2 or less.
- the core material 12 is a member used as a core of the door structure 10.
- the core 12 has a flat plate shape and has a first surface 12 A and a second surface 12 B facing each other.
- the flat plate shape is a shape that has two main surfaces with a large area relative to the thickness.
- the core material 12 is a member used as a core of the door structure 10, it is preferable that the core material 12 has rigidity.
- the core 12 may be made of wood, metal, resin, or a composite material thereof. The material can be appropriately selected according to the characteristics required for the door structure 10.
- a material such as a medium density fiberboard such as a wood fiber board, plywood, or particle board is used as the core material 1 2 Can be used as appropriate.
- MD F Medium Density Fiberboard
- Plywood is constructed by stacking multiple veneers.
- Particleboard is manufactured by heat-pressing small pieces of wood using an adhesive and is specified in J I S A 5908.
- a so-called solid structure such as a wood fiber board, plywood, or particle board
- a flash structure board can be applied as the structure.
- the flash structure board has a hollow structure in which a frame is made of wood and plywood is attached to both sides. The density can be reduced compared to the solid structure.
- the density of the wooden core material 12 is preferably 400 kg/m 3 or more and 900 kg/m 3 or less. If the density of the core material 12 is 400 kg/m 3 or more, the strength of the core material 12 can be secured. If the core material 1 2 has a density of 900 kg/m 3 or less, the door ⁇ 0 2020/175397 6 ⁇ (: 170? 2020 /007191
- the structure 10 can be made lighter.
- the density of the wood core 1 2 is
- the specific gravity of the core material 12 is 0
- the metal core material 12 for example, a metal material such as aluminum or iron can be appropriately used as the core material 12.
- resin core material 12 for example, acrylonitrile-butadiene-styrene copolymer synthetic resin (Mitsumi 3 resin), polyvinyl chloride resin ( ⁇ resin), or acrylic resin may be used as the core material 12 as appropriate. Can be used.
- Mitsubishi 3 resin acrylonitrile-butadiene-styrene copolymer synthetic resin
- ⁇ resin polyvinyl chloride resin
- acrylic resin acrylic resin
- the plate thickness of the core material 12 is appropriately selected according to the thickness of the door structure 10.
- the thickness of the core materials 1 and 2 is The following is preferable.
- the thickness of the core material 12 is more preferably the above, more preferably 501 01 or more, and particularly preferably 110 111 111 or more.
- the thickness of the core 12 is 20 The following is more preferable
- the plate-shaped body 16 is a brittle material, the effects of the present invention can be enjoyed. Brittleness means the property of breaking easily when subjected to a force.
- the material of the plate-shaped body 16 include a glass plate, a resin plate and a ceramic plate.
- the resin plate is preferably a brittle resin plate.
- the brittle resin plate include a melamine resin plate, an acrylic resin plate, a polycarbonate resin plate, and a vinyl chloride plate.
- the ceramic plate include ceramic members such as tiles.
- the plate-shaped body may be made of stone. The case where the plate-shaped body 16 is a glass plate will be described below.
- the glass plate applied to the plate-shaped body 16 is not particularly limited in terms of the type of glass.
- soda lime glass, non-alkali glass, aluminosilicate glass and the like can be mentioned.
- aluminosilicate glass containing eight ⁇ 2 ⁇ 3 3% or more by mass percent on the oxide basis is preferred.
- the glass plate has a thickness of 0.5.
- the following are preferred.
- Glass plate thickness is 0.5 With the above, the warp of the core material 12 can be absorbed. 5 glass plates ⁇ 0 2020/175397 7 ⁇ (: 170? 2020 /007191
- the plate thickness of the glass plate is more preferably 1 111 01 or more, 1. The above is more preferable.
- the thickness of the glass plate is 4 The following is more preferable, and 3 01 01 or less is further preferable.
- the density of the glass plate is
- the specific gravity of the plate-like body 16 is preferably 2.3 or more and 2.8 or less, and more preferably 2.4 or more and 2.6 or less.
- the glass plate applied to the plate-shaped body 16 is preferably in close contact with the design layer 18.
- the design layer 18 is viewed through the plate-shaped body 16 by closely contacting it, the door structure 10 is more aesthetically pleasing because of the increased depth and luxury.
- the visible light transmittance of the glass plate based on the standard eight light sources (" 3 Required in accordance with 3106
- the upper limit of the visible light transmittance based on the standard eight light sources of the glass plate is not particularly limited, but may be 100% or less, may be 92% or less, and may be 90% or less. Good.
- the glass plate may be subjected to a texture treatment by post-processing such as frosting, in order to provide the surface with a texture.
- the glass plate can be manufactured by a known method. That is, a glass plate is manufactured by cutting a glass formed into a ribbon by a float method, a fusion method, a downdraw method, a mouth-out method or the like.
- the glass plate may have a compressive stress layer on its surface. When the glass plate is tempered, it becomes a tempered glass plate.
- the tempered glass sheet that has been subjected to the tempering treatment is less likely to break than when it is not tempered.
- the tempered glass sheet includes a compressive stress layer on the surface layer, that is, a front surface layer and a back surface layer having residual compressive stress, and an intermediate layer formed between the front surface layer and the back surface layer and having residual tensile stress.
- the residual compressive stress decreases from both ends of the tempered glass plate in the plate thickness direction, and residual tensile stress occurs inside the tempered glass plate.
- the end face of the tempered glass plate may be continuously covered with the residual compressive stress on the front surface layer and the back surface layer. Since the end surface of the tempered glass plate is covered with the residual compressive stress, it is difficult for the tempered glass plate to be cracked by an impact, which is preferable.
- the end face of the tempered glass plate is not covered with the residual compressive stress, and the end face of the intermediate layer may be exposed on the end face of the tempered glass plate. In that case, it is preferable that it is covered with a cover material such as resin.
- the tempered glass plate is manufactured by subjecting it to a tempering treatment to generate residual compressive stress on the front and back surfaces of the glass plate.
- the tempered glass plate may be either a chemically strengthened glass obtained by a chemical strengthening treatment such as an ion exchange method or a physically strengthened glass obtained by a physical strengthening treatment such as an air cooling strengthening method.
- the chemical strengthening treatment the value of the residual compressive stress in the front surface layer and the back surface layer can be increased even if the glass plate is thinner.
- the value of the residual compressive stress in the surface layer is preferably 300 IV! 3 or more, more preferably 400 IV! 3 or more.
- the upper limit of the residual compressive stress in the surface layer is not particularly limited, but it may be 1 200 1 ⁇ /1 3 or less, or 8 0 0 1 ⁇ /1 3 or less. ⁇ /1 It may be 3 or less.
- the thickness of the compression stress layer may be 50 or less, or 40 or less.
- the thickness of the compressive stress layer may be 10 or more, or 20 or more.
- the front surface and the back surface of a glass plate are ion-exchanged, and ions having a small ion radius (eg, !_ ⁇ ion, N 3 ion) contained in glass are exchanged with ions having a large ion radius (eg, ⁇ ion).
- ions having a small ion radius eg, !_ ⁇ ion, N 3 ion
- ions having a large ion radius eg, ⁇ ion
- the air-cooling strengthening method is to cool a glass plate at a temperature near the softening point from both sides and to make a temperature difference between the front surface and the back surface of the glass plate and the inside of the glass plate. Residual compressive stress can be generated on the back surface.
- the time required for the strengthening treatment is from several seconds to several tens of seconds. ⁇ 02020/175397 9 ⁇ (: 170? 2020 /007191
- the productivity is much better than the chemical strengthening method such as the substitution method.
- the plate-shaped body 16 may have a functional layer for adding a special function, on the surface opposite to the resin layer 14.
- the functional layer include an antifouling film, an antibacterial film or an antifogging film.
- the antifouling film has the effects of reducing the adhesion of fingerprints and making it difficult for dirt to attach.
- fingerprints adhere to the surface of the plate-like body 16 and impair the design, so it has an AFP (Anti-Finger Print) function to reduce the adhesion of fingerprints.
- the AFP function adheres the AFP agent to the plate-like body 16 to form an AFP film on the glass plate.
- the A F P agent include fluorine-containing organosilicon compounds.
- the fluorine-containing organic silicon compound may be used without particular limitation as long as it imparts antifouling property, water repellency and oil repellency.
- the molecular weight of the AFP agent is preferably 3,000 or more and 100,000 or less, more preferably 3,000 or more and 8,000 or less, and further preferably 3,000 or more and 6,000 or less.
- the molecular weight of the AFP agent is 3,000 or more, flexibility is imparted to the molecular structure, and scratch resistance and surface slipperiness can be obtained. Further, when the amount is 10,000 or less, the number of reactive groups per molecule of the AFP agent can be sufficiently secured, and the adhesion with the surface of the plate-shaped body 16 can be secured.
- the antibacterial film is formed by adhering an antibacterial agent that exhibits antibacterial properties to the plate-shaped body 16.
- the antibacterial agent include natural antibacterial agents such as wasabi, metallic antibacterial agents such as copper and silver, and oxide antibacterial agents such as titanium oxide.
- a solution containing silver is applied to the plate-shaped body 16 to form a silver film, and the plate-shaped body on which the silver film is formed is subjected to heat treatment, so that silver ions are introduced from the surface of the plate-shaped body 16 to the inside. Is preferable from the viewpoint of the durability of the effect.
- the antifogging film is provided with a water-absorbent resin layer on the surface of the plate-shaped body 16 and absorbs and removes minute water droplets formed on the plate surface of the plate-shaped body 16 to remove It has the effect of preventing the surface of 6 from becoming cloudy and maintaining its design.
- the antifogging film includes, for example, a base layer and a water absorbing layer.
- the underlayer is for making it difficult for the water absorption layer to peel off from the glass plate. ⁇ 2020/175397 10 10 (: 170? 2020/007191
- the water absorbing layer is obtained by applying a composition containing a raw material component of a cured resin selected from a cured epoxy resin, a urethane resin and a crosslinked acrylate resin onto the underlayer and reacting it.
- the Young's modulus of the plate-shaped body 16 is preferably 5° 3 or more.
- the Young's modulus of 6 is 5° 3 or more, it is hard to warp.
- the Young's modulus of the plate-like body 16 is more preferably 10° 3 or more, further preferably 300 9 a or more, and particularly preferably 50° 3 or more.
- the upper limit of the Young's modulus of the plate-shaped body 16 is not particularly limited, it may be 100° C. or less.
- a design layer 18 is formed between the plate-like body 16 and the resin layer 14.
- the design layer 18 is formed, for example, by applying a coating material containing a coloring pigment on the surface of the glass plate that is the plate-shaped body 16 and then drying and curing it.
- the paint include acrylic resin-based paint. Acrylic resin-based paints have high adhesion and excellent weather resistance and corrosion resistance. It is also preferable in that the finish is beautiful.
- the design layer 18 is not particularly limited as long as it can impart design properties, and may be, for example, a melamine resin-based paint or an epoxy resin-based paint, and the coloring pigment may have various colors. ..
- the design layer 18 may be a mirror coated with a metal film.
- the method of applying the coating material is not particularly limited, and for example, a mouth coating method, a spray coating method, a dip coating method, a flow coating method, a screen printing method, a spin coating method and the like are used.
- the design layer 18 formed into a sheet shape may be attached to the glass plate which is the plate-like body 16 with an adhesive or the like.
- the design layer 18 formed into a sheet may have a single color or a plurality of colors, or may have a pattern such as a natural stone tone or a brick tone.
- the design layer 18 may be provided with design properties by, for example, a template glass in which a pattern is provided on the surface of the plate-like body 16 by unevenness or the like. ⁇ 2020/175397 1 1 ⁇ (: 170? 2020/007191
- the resin layer 14 is composed of a resin layer that is a foam containing a skeletal resin that defines cells (cells).
- a crosslinking agent is added to the skeletal resin, and a crosslinking reaction by the crosslinking agent and a decomposition reaction of the foaming agent are caused to cause the gas component to stay, Bubbles (cells) are defined, and a resin layer 14 having a predetermined foaming property is obtained.
- the kind of skeleton resin and the manufacturing method are not limited as long as a predetermined foaming property can be obtained.
- a synthetic resin, a synthetic rubber or the like can be used, and examples thereof include polyethylene, an ethylene-vinyl acetate copolymer (EVA: Ethylene-Vinyl Acetate), an ethylene-propylene-gen rubber (EVA). EPDM), silicone, polyurethane, etc. can be used.
- the bubbles defined by the skeleton resin are preferably closed cells.
- An independent bubble means a structure in which bubbles are arranged independently of each other.
- the skeleton resin of the resin layer 14 preferably contains a flame retardant. Ignition of the resin layer 14 is suppressed by the flame retardant.
- each of the organic flame retardant and the inorganic flame retardant can be added to the skeleton resin alone or in a mixture.
- a brominated aromatic compound such as a phosphorus compound can be used.
- the inorganic flame retardant magnesium hydroxide, aluminum hydroxide or the like can be used.
- the mass ratio (flame retardant/skeleton resin) of the flame retardant contained in the resin layer 14 to the skeleton resin is preferably 20% or more, more preferably 27% or more, and 30% or more. Is more preferable, 50% or more is particularly preferable, and 70% or more is most preferable.
- the upper limit of the mass ratio of the flame retardant contained in the resin layer 14 to the skeleton resin is not particularly limited, but may be 100% or less, or 80% or less. Well, it can be less than 70%. ⁇ 2020/175397 12 12 (: 170? 2020 /007191
- Layer 1 4 has a thickness of 1 If it is above, the warp of the core material 12 can be absorbed and sufficient impact strength can be obtained when laminated with the plate-shaped body 16.
- the thickness of the resin layer 14 is more preferably 2 111 01 or more, still more preferably 310 1! or more.
- Resin layer When it is below, the deformation of the resin layer 14 due to the load of the plate-shaped body 16 is suppressed, and the shape of the door structure 10 is hard to change.
- the thickness of resin layer 14 is 7 The following is more preferable, The following is more preferable.
- the density of the resin layer 14 is Is preferred. Resin layer Sufficient impact strength can be obtained when laminated with the plate-like body 16.
- the resin layer 14 has a density of 70! ⁇
- the door structure 10 can be made lighter if: Density of the resin layer 1 4 1 2 0 1 ⁇ 9 / ⁇ 1 3 hereinafter more, more preferably from 1 hundred 1 ⁇ 9/3 or less, particularly preferably 8 0 1 ⁇ 9 / ⁇ ⁇ or less.
- the specific gravity of the resin layer 14 is preferably 0.03 or more and 0.16 or less.
- the Shore 8 hardness of the resin layer 14 is preferably 10 or more and 60 or less.
- the Shore 8 hardness is based on the measurement value of a durometer (Asker rubber hardness tester type 8 manufactured by Asker Co.). Push the indenter (pushing needle) into the surface of the object to be deformed, measure the amount of deformation (pushing depth), and use it as the average value of at least 4 points. If the resin layer 14 is thin and soft, measure it by overlapping the resin layers so that the thickness is 6 to 12. When the Shore hardness is 10 or more, the workability is good because it has sufficient rigidity, and since the resin layer 3 is difficult to deform, the plate-shaped body 16 is difficult to deform and crack.
- the Shore 8 hardness is more preferably 20 or more, and further preferably 30 or more. Further, if the Shore 8 hardness is 60 or less, the plate-shaped body 16 is hard to crack even if it receives a strong impact because it has sufficient shock absorption. The Shore 8 hardness is more preferably 50 or less.
- the resin layer 14 may include other components.
- Other components may include, for example, pigments and inorganic additives.
- Various functions can be added to the resin layer 14 ⁇ 0 2020/175397 13 ⁇ (: 170? 2020 /007191
- the resin layer 14 has a flame retardant, for example, is I (Infrared spectroscopy) ⁇ ⁇ ⁇ (Thermogravimetric analysis) ⁇ 0 (Differential scanning calorimetric analysis) and the like.
- the resin layer 14 may be a plate-shaped member, or may be integrally molded with the plate-shaped body 16 by injection molding or extrusion molding.
- the resin layer 14 is a plate-shaped member, the plate-shaped body 16 and the plate-shaped resin layer 1 4 are arranged so that the design layer 18 is interposed between the plate-shaped body 16 and the resin layer 14. It is preferable that the and are adhered with an adhesive, a pressure-sensitive adhesive (hereinafter, including the pressure-sensitive adhesive, referred to as a plate-shaped adhesive).
- the adhesive for the plate-shaped body may be applied to the entire surface of the resin layer 14 or may be a part thereof. It is advantageous to apply the adhesive to the entire surface because the plate-shaped body 16 is less likely to break. Also, an adhesive may be applied to the design layer 18 of the plate-shaped body 16.
- a general architectural sealing material can be used, and examples thereof include modified silicone sealing material, acrylic adhesive and synthetic rubber adhesive.
- the adhesive may be in the form of a sheet such as a double-sided tape. In addition, it is suitable as a building material to select materials and coating amounts so that the adhesive has high noncombustibility.
- the adhesive area between the plate-shaped body 16 and the plate-shaped resin layer 14 is The area is preferably 10% or more, more preferably 50% or more, further preferably 90% or more,
- the upper limit of the adhesion area between the plate-shaped body 16 and the plate-shaped resin layer 14 is not particularly limited, but may be 100% or less of the area of the plate-shaped body.
- the plate-shaped body 16 on which the design layer 18 is formed is placed in a molding die and the resin is placed on the design layer 18. Is injected and integrally molded.
- the resin is supplied onto the design layer 18 of the plate-like body 16 from the extrusion mold and cured to be integrally molded.
- the resin layer 14 may be integrally molded after applying an adhesive or an undercoat (primer), for example, a silane coupling agent, on the plate-shaped body 16 side.
- the resin layer 14 and the core material 12 are preferably bonded together via an adhesive (referred to as an adhesive for core material).
- an adhesive for core material acrylic adhesive, synthetic rubber, silicone, or modified silicone can be used.
- a double-sided tape may be used as the adhesive for the adhesive system.
- the door structure 10 of the first embodiment has the resin layer 14 between the plate-shaped body 16 and the core material 12, it has the following advantages.
- core material 12 is made of, for example, wood, it absorbs moisture and is easily warped.
- Core material 1 is made of, for example, wood, it absorbs moisture and is easily warped.
- the right side of the above formula is preferably 10%, more preferably 15%, and further preferably 20%.
- the specific gravity of the resin layer 14 is smaller than the specific gravity of the core material 12 and the plate-shaped body 16.
- a part of the core 12 and the plate 16 is partially covered with the resin layer 14 By doing so, the specific gravity of the entire door structure 10 can be reduced, so that the door structure 10 can be made lighter, as will be shown in the examples described later.
- the specific gravity of the door structure 10 is preferably 1.8 or less. If the specific gravity of the door structure 10 is 1.8 or less, the weight of the door structure 10 can be reduced.
- the specific gravity of the door structure 10 is more preferably 1.5 or less, further preferably 1.2 or less, particularly preferably 1.0 or less, most preferably 0.9 or less.
- the door structure 10 of the first embodiment is preferably used as a door for opening storage furniture.
- FIG. 2 is a schematic sectional view showing a door structure 20 as an example of the second embodiment.
- the door structure 20 includes a core member 22, a first resin layer 24, and a first plate-like member 26. ⁇ 2020/175397 15 15 (: 170? 2020/007191
- a laminated body 33 including a second resin layer 30 and a second plate-shaped body 3 2.
- the core material 22 has a flat plate shape having a first surface 22 and a second surface 22 which face each other. It should be noted that it is possible to arbitrarily determine which of the two main surfaces of the core material 22 facing each other is the first surface 2 28 and the second surface 22 2.
- the first resin layer 24 is a resin layer which is a foam, and is arranged on the first surface 22 8 side of the core material 22.
- the first plate-like body 26 is a brittle plate-like body having a design property, and is arranged on the surface of the first resin layer 24 opposite to the core material 22.
- the core material 22 and the first plate-like body 26 are arranged at positions facing each other with the first resin layer 24 interposed therebetween.
- the first design layer 28 is arranged between the first plate-like body 26 and the first resin layer 24.
- the second resin layer 30 is a resin layer that is a foam, and is arranged on the second surface 22 side of the core material 22.
- the second plate-shaped body 32 is a brittle plate-shaped body having a design property, and is arranged on the surface of the second resin layer 30 opposite to the core material 22.
- the core material 22 and the second plate-shaped body 32 are arranged at positions facing each other with the second resin layer 30 interposed therebetween.
- the second design layer 34 is disposed between the second plate-shaped body 32 and the second resin layer 30.
- the door structure 20 includes the first design layer 28 and the second design layer 34, the door structure 20 can produce a high-class aesthetic appearance when used as an entrance/exit of a building.
- the total thickness of the door structure 20 of the second embodiment is The following is preferable.
- the total thickness of the door structure 20 of the second embodiment is more preferably 20 or more, More preferable, 30 The above is particularly preferable. Further, the total thickness of the door structure 20 of the second embodiment is more preferably 45 or less, The following is more preferable.
- the entire first surface 22 8 and second surface 22 2 of the core 2 2 are covered with the resin layer and the plate-like body.
- a part of the first surface 222 and the second surface 22 of the core material 22 may be covered with the resin layer and the plate-like body.
- the ratio of the area covered by the resin layer and the plate-like body is preferably 80% or more, and 9 0% or more is more preferable, and 95% or more is further preferable.
- the resin layer and the plate-like body ⁇ 02020/175397 16 ⁇ (: 170? 2020 /007191
- the percentage of the covered area may be 100% or less, or 97% or less.
- the area of the door structure 20 of the second embodiment ⁇ . 01 2 or more, 0.5 more preferably 1, ⁇ . 5 2 or more, and particularly preferably 1 2 or more, 2.5 2
- the above is the most preferable.
- the large area of the door structure 20 makes it more likely to warp and becomes heavier, but the presence of the resin layer alleviates the warpage and makes it lighter.
- the area of the door structure 20 of the second embodiment may be 5 2 or less, may be four 2 or less, 3. may be 5 2 or less, 3_Rei_1 2 hereinafter with It may be.
- the core material 22 is a member used as a core of the door structure 20.
- the core material 22 has a flat plate shape and has a first surface 22 and a second surface 22 facing each other.
- the same material and structure as the core material 12 of the first embodiment can be applied.
- the core material 22 having a thick plate thickness from the viewpoint of increasing the rigidity of the laminated body.
- the first plate-like body 26 and the second plate-like body 32 are the same as the plate-like body 16 of the first embodiment. ⁇ 2020/175397 17 ⁇ (: 170? 2020/007191
- the first plate-like body 26 and the second plate-like body 32 can be made of the same material or different materials, and can be made to have the same plate thickness or different plate thicknesses.
- the same design layers as the design layer 18 of the first embodiment can be applied.
- the first design layer 28 and the second design layer 34 can be composed of the same design layer or different design layers.
- the same aesthetics or different aesthetics can be provided on the first surface 2 2 side and the second surface 22 2 side of the core material 22 of the door structure 20.
- the same resin layer as the resin layer 14 of the first embodiment can be applied to the first resin layer 24 and the second resin layer 30.
- the first resin layer 24 and the second resin layer 30 can be made of the same material or different materials, and can have the same thickness or different thickness.
- the door structure 20 of the second embodiment has a first resin layer 24 between the first plate-like body 26 and the core material 22 and a second plate-like body 3 2 and the core material 2 2. Since the second resin layer 30 is provided between the first resin layer and the second resin layer, the following advantages are achieved.
- core material 22 is made of, for example, wood, it absorbs moisture and is easily warped.
- Core material 2 is made of, for example, wood, it absorbs moisture and is easily warped.
- the warp of the core material 2 2 can be alleviated by the deformation of the first resin layer 24 and the second resin layer 30 of the door structure 20.
- the flatness of the first plate-like body 26 and the second plate-like body 32 can be realized, so that the designability of the first plate-like body 26 and the second plate-like body 32 can be secured.
- the core member 2 2 is a warp amount when the single and 1 to 0, and the warpage of the laminate 3 3!!! And can satisfy the following expression.
- the specific gravities of the first resin layer 24 and the second resin layer 30 are smaller than the specific gravities of the core material 22, the first plate-like body 26, and the second plate-like body 32.
- the door structure 20 has a uniform thickness ⁇ 0 2020/175397 18 18 (: 170? 2020 /007191
- the core material 2 2, the first plate-shaped body 26, and the second plate-shaped body 2 Since the specific gravity of the entire door structure 20 can be reduced by making a part of the body 32 into the first resin layer 24 and the second resin layer 30, as shown in Examples described later, 20 can be made lighter.
- the specific gravity of the door structure 20 is preferably 1.8 or less. If the specific gravity of the door structure 20 is 1.8 or less, the weight of the door structure 20 can be reduced.
- the specific gravity of the door structure 20 is more preferably 1.5 or less, further preferably 1.2 or less, particularly preferably 1.0 or less, and most preferably 0.9 or less.
- the door structure 20 of the second embodiment is preferably used as a door for a doorway of a building.
- the door structure of the third embodiment includes a molding material on the end surface of the laminated body.
- the door structure of the third embodiment can improve the strength and design of the end surface of the door structure.
- FIG. 3 is a perspective view of the door structure 10 according to the third embodiment.
- the door structure 10 includes a core material 12, a resin layer 14 and a laminated body 17 including a plate-like body 16.
- the laminate 17 has four end faces 17.
- the door structure 10 includes a molding material 60 that covers the end surface 17 of the laminated body 17.
- FIG. 3 shows that only one molding material 60 covers the end surface 17, the molding material 60 basically covers all the end surfaces 17.
- the molding material 60 is made of, for example, a material selected from the group consisting of acrylonitrile-butadiene-styrene copolymerization synthetic resin, acrylic resin, and polyethylene terephthalate resin.
- the molding material 60 covers the end surface 178 of the laminate 17 so that the molding material 60 protects the end surface 178.
- the molding material 60 suppresses damage to the end surface 17 such as cracking and chipping.
- Fig. 4 is a schematic cross-sectional view of a part of the end face 178 taken along a plane orthogonal to the main surface of the door structure 10 of Fig. 3. As shown in FIG. 4, the end face 17 78 of the laminated body 17 and the molding material 60 are bonded by the adhesive 62. Adhesive 6 2 is ⁇ 0 2020/175397 19 ⁇ (: 170? 2020/007191
- Hot Tomeruto adhesives are, for example, specific temperature (1 0 0 ° ⁇ ⁇ 2 5 0 ° ⁇ ) heating, an adhesive used in melted.
- ethylene vinyl acetate resin 8) type adhesive, polyolefin resin type adhesive, and polyurethane resin) type adhesive can be used as the hot melt adhesive.
- the end face 17 of the laminated body 17 is configured to be flush.
- flush means that the step difference between the respective end faces of the core material 12, the resin layer 14 and the plate-shaped body 16 that constitute the laminated body 17 is ⁇ 0.5. It means within the range. Since the end face 17 of the laminate 17 is flush, the adhesive 62 can be formed with a uniform thickness. Therefore, the adhesive strength between the end face 178 and the molding material 60 can be improved.
- the thickness of the plate-shaped body 16 can be made smaller than that of a single plate-shaped body without the resin layer. ..
- the plate-shaped body 16 is a transparent and thin glass plate, it becomes difficult for a person to visually recognize the adhesive 62 from the end face of the plate-shaped body 16. Since the adhesive 62 is not visible, the design of the door structure 10 can be improved.
- the end face 11 of the laminated body 17 is compared with a single plate-shaped body without the resin layer. It can improve the adhesive strength with the string material 60.
- the adhesive strength between the adhesive 62 and the resin layer 14 is higher than the adhesive strength between the adhesive 62 and the plate-shaped body 16. Therefore, as compared with a single plate-shaped body having no resin layer, the presence of the resin layer 14 enables the adhesive material 62 to firmly bond the molding material 60 and the resin layer 14 together.
- FIG. 5 is a schematic cross-sectional view of a part of the door structure 20 according to another mode of the third embodiment.
- the door structure 20 is a laminated body 3 including a core material 22, a first resin layer 24, a first plate-like body 26, a second resin layer 30 and a second plate-like body 3 2. 3 and The end face 33 8 of the laminate 3 3 and the molding material 60 are bonded by the adhesive 62.
- a door structure 20 according to another form of the third embodiment has the same effects as the door structure 10 of the third embodiment.
- FIGS. 6 to 9 The method of manufacturing a fitting according to this embodiment will be described with reference to the door structure 10 of the first embodiment and the third embodiment.
- a core material 12 a first resin layer 14 and a first plate-shaped body 16 are prepared.
- the resin layer 14 and the plate-shaped body 16 have substantially the same area. Therefore, the end surface of the resin layer 14 and the end surface of the plate-shaped body 16 are flush with each other.
- the areas are the areas of the main surface of the resin layer 14 and the main surface of the plate-shaped body 16.
- the area of the core material 12 is larger than the areas of the resin layer 14 and the plate-shaped body 16.
- the core material 12 projects from the resin layer 14 and the plate-shaped body 16.
- the end faces 17 of the laminate 17 are not flush with each other.
- the cutting blade 70 cuts the core material 12 and a part of the resin layer 14 along the end face of the plate-shaped body 16.
- the cutting blade 70 completely cuts the core material 12.
- the cutting blade 70 cuts a part of the resin layer 14 and leaves the resin layer 14 at a distance of 8 from the plate-shaped body 16 side. Therefore, since the cutting blade 70 does not come into contact with the plate-shaped body 16, it is possible to protect the plate-shaped body 16 from damage caused by the cutting blade 70.
- the cut projecting portions of the core material 12 are removed, and the end faces 17 of the laminate 17 are flush with each other.
- a door structure 10 is manufactured in which the end faces 17 of the laminate 17 are flush.
- the molding material 60 is attached to the end face 17 of the laminated body 17 of the door structure 10.
- the molding material 60 is attached to the end face 178 of the laminated body 17 by, for example, an edge bonding machine (edge bander), and the door structure 10 shown in FIG. 3 is manufactured.
- edge bonding machine edge bander
- the edge sticking machine (not shown) is, for example, a transport unit for transporting the door structure 10, an application unit for applying the hot melt adhesive to the end face 17 and a pressing material for attaching the molding material 60. It has a unit and so on.
- the adhesive is applied to the end face 17 by the coating unit, and then the molding material 60 is attached to the end face 1 78 by the pressing unit. In this way, the molding material 60 is attached to one end face 1 78 of the laminated body 17. In the same manner, molding material 60 is attached to the remaining three end faces 1780.
- the end face 17 is flush with the cutting blade 70.
- the molding material 60 can be attached using the edge pasting machine.
- the end faces cannot be flush with each other as described above, and therefore, a molding machine using an edge sticking machine is used. It was difficult to attach the material.
- the door structure 10 of the embodiment enables the use of the rimming machine.
- a warp absorbency test was conducted in order to confirm the relaxation of the warp of the core material.
- the laminated body 31 having the core material 12 and the glass plate ⁇ is placed on the flat surface 50 with the side of the core material 12 and the center portion of the long side of the laminated body 31.
- a spacer 52 parallel to the short side was inserted between the flat surfaces 50.
- the core member 1 2 of warpage 1-1 1 0.
- the multiple spacers 52 used in the calculation of were used.
- the warp amount of the laminated body 31! I 1 was determined by using the glass plate of the flat laminated body 31 before the spacer 52 as a reference plane and the spacer 52 from the reference plane. It was determined by measuring the distance to the top of the later warped laminate 31.
- the laminated body 32 having the core material 12 is placed on the flat surface 50, and a space parallel to the short side is provided between the central portion of the long side of the laminated body 32 and the flat surface 50. I put in 52.
- the warpage amount of the core material 12 in FIG. 10 is 1 to 1.
- the warp amount 1 to 1 ! of the laminated body 32 is based on the flat laminated glass plate 32 before the spacer 52 is kneaded as the reference surface, and the spacer 52 is kneaded from the reference surface. It was determined by measuring the distance to the top of the warped laminate 32 after the heating.
- the laminate shown in FIG. 12 constitutes the laminate of the embodiment.
- the amount of warpage of the core material 12 is 1 to 1.
- warpage of specimens five laminate !!! the determined Me was calculated absorptance (%) by the following equation.
- Table 1 shows the door structure and the amount of warp! ⁇ I. , The amount of warp ! ! , absorption rate, shear stress, and stress relaxation rate.
- Examples 1, 6 and 11 do not include the resin layer 14. As a result, the absorption rate is less than 5%.
- Example 7 to Example 10 and Examples 12 to 15 including the resin layer 14 the absorption rate of 5 (%) or more can be achieved.
- the thickness of the resin layer 14 increases, ⁇ 0 2020/175397 24 ⁇ (: 170? 2020 /007191
- the door structure the maximum value of the shear stress generated at the bonding interface between the glass plates, anti-Ri amount 1 to 0 of shear stress generated in the glass sheet when bonding the glass plate alone on core material
- the maximum value 0 and the stress relaxation rate are shown in Table 1.
- the shear stress generated at the adhesive interface of the glass plate is (1 ⁇ /1) / (2 X 1), IV! is the bending moment,
- the stress relaxation rate is calculated by the following formula.
- Example 2 to Example 5, Example 7 to Example 10 and Example 12 to 15 including the resin layer 14 can achieve a stress relaxation rate of 5 (%) or more. Further, it can be understood that the stress relaxation rate increases as the thickness of the resin layer 14 increases. Since the door structures of Examples 2 to 5, Example 7 to Example 10 and Examples 12 to 15 include the resin layer 14, the shear stress generated at the bonding interface of the glass plate is small, and Hard to peel off from the core material.
- Specific gravity was calculated for the door structure of the first embodiment. IV! 0 (specific gravity: 0.8) or flash structure plate (specific gravity: 0.5) as the core material, and polyethylene (specific gravity: 0.07) as the resin layer.
- a glass plate (specific gravity: 2.5) as a plate-like body to form a door structure.
- Table 2 is a table in which the specific gravity is calculated when IV! 0 is used as the core material
- Table 3 is a table in which the specific gravity is calculated when the flash structure plate is used as the core material. The specific gravity was calculated by the following formula.
- Example 16-Example 20 Is the thickness of the core material The door structure which changed the thickness of a resin layer and the thickness of a glass plate is shown.
- the resin layer ⁇ 0 2020/175 397 25 ⁇ (: 170? 2020 /007191
- the thickness of 0.0 (111 111) and the thickness of glass plate 0.0 (01 01) mean that they are not provided.
- Examples 21 to 25 show door structures in which the total thickness is 17 and the thickness of the resin layer and the thickness of the glass plate are changed.
- Example 26 to Example 30 ( ⁇ [3 ⁇ 43) have a total thickness of 20 and have a door structure in which the thickness of the resin layer and the thickness of the glass plate are changed.
- Example 20 that is a door structure composed of a core material and a glass plate
- Example 30 had the highest specific gravity within each group.
- the specific gravity was the second from the bottom in each group ( ⁇ [3 ⁇ 4 1).
- the amount of warp is not reduced.
- Example 1 which is an Example 17 to Example 19, Example 22 to Example 24, Example 2 7 to Example 29
- Example 1 which is a door structure of a combination of the resin layer 1 and the glass plate 5
- the specific gravity of 8, Example 2 3 and Example 2 8 is Was the largest among the examples. It is composed of 1 0 111 111 resin layers and 0.50! ⁇ 0 2020/175 397 26 ⁇ (: 170? 2020 /007191
- the specific gravity of the door structure of the embodiment according to the embodiment, Example 24, and Example 29 is the smallest among the examples of each group ( ⁇ .
- Door structure of the example (Examples 17 to 19) , Example 22 to Example 24, Example 27 to Example 29) had a specific gravity of 1.8 or less.
- Examples 31 to 35 show the door structure in which the thickness of the core material is changed and the thickness of the resin layer and the thickness of the glass plate are changed.
- Examples 36 to 40 show the door structure in which the total thickness is 17 and the thickness of the resin layer and the thickness of the glass plate are changed.
- Examples 41 to 45 show a door structure in which the total thickness is 2001111 and the thickness of the resin layer and the thickness of the glass plate are changed.
- Example 35, Example 40, and Example 45 which have a door structure composed of a core material and a glass plate, had the highest specific gravity in each group. .. Example 3 1, Example 3 6, and Example 41 with core material only
- Example 32 to Example 34, Example 37 to Example 39, and Example 42 to Example 44 which are Examples, the resin layer of 1 and The specific gravity of Example 3 3, Example 3 8 and Example 4 3 which are the door structure of the combination of the glass plates of was the largest among the examples.
- the specific gravities of the examples 3 4, example 39, and example 4 4 of the door structure of the embodiment composed of the resin layer of 1 0 111 111 and the glass plate of 0. was the smallest of all the examples.
- the door structure (Example 32 to Example 34, Example 37 to Example 39, Example 42 to Example 44) of the example had a specific gravity of 1.8 or less.
- Specific gravity was calculated for the door structure of the second embodiment. 1 ⁇ /10 as core material (specific gravity: 0.8) or flash structure plate (specific gravity: 0.5), polyethylene as resin layer (specific gravity: 0.07), and glass plate as plate ( Specific gravity: 2.5) was combined to form a door structure.
- Table 4 is a table for calculating the specific gravity when IV! 0 is used as the core material
- Table 5 is a table for calculating the specific gravity when the flash structure plate is used as the core material.
- Example 46-Example 50 Is the total thickness
- the door structure in which the thickness of the resin layer and the thickness of the glass plate are changed is shown.
- the door structure of the second embodiment includes two resin layers and two glass plates sandwiching the core material.
- the thickness of the resin layer in Table 4 is the total thickness of the two resin layers
- the thickness of the glass plate is the total thickness of the two glass plates.
- Example 50 which is a door structure composed of a core material and a glass plate, ⁇ 0 2020/175 397 28 ⁇ (: 170? 2020 /007191
- Examples 47 to 49 which are working examples, 2 With a resin layer of 1
- the specific gravity of the example 48 that is the door structure of the combination of glass plates of It was the largest of the seven examples. 2 0 111 111 resin layer and 1.0
- the example of the door structure of the embodiment composed of the glass plate of 7 was the smallest.
- the door structure (Example 47 to Example 49) of the example had a specific gravity of 1.8 or less.
- Examples 5 1 to 5 5 ( ⁇ [3 ⁇ 4 8) The door structure in which the thickness of the resin layer and the thickness of the glass plate are changed is shown.
- the thickness of the resin layer in Table 5 is the total thickness of the two resin layers, and the thickness of the glass plate is the total thickness of the two glass plates.
- Example 55 which has a door structure composed of a core material and a glass plate, had the largest specific gravity in Group 0 [3 ⁇ 48.
- the amount of warpage is not reduced.
- Examples 47 to 49 which are working examples, 2 With a resin layer of 1
- the specific gravity of example 53 which is a door structure with a combination of glass plates of It was the largest of the seven examples. 2 0 111 111 resin layer and 1.0
- the example 5 4 of the door structure of the embodiment composed of the glass plate of No. 4 has the smallest specific gravity in Group No. 8.
- the door structure (Example 47 to Example 49) of the example had a specific gravity of 1.8 or less.
Landscapes
- Engineering & Computer Science (AREA)
- Civil Engineering (AREA)
- Structural Engineering (AREA)
- Securing Of Glass Panes Or The Like (AREA)
Abstract
芯材の反りを緩和でき、かつ軽量化できる建具、及び建具の製造方法を提供する。 建具は、対向する第1面と第2面とを有する平板形状の芯材と、芯材の第1面の側に配置された発泡体である第1樹脂層と、第1樹脂層の、芯材とは反対側の面に配置された意匠性を有する脆性の第1板状体とを含む積層体、を備える。
Description
\¥0 2020/175397 1 卩(:17 2020 /007191 明 細 書
発明の名称 : 建具、 及び建具の製造方法
技術分野
[0001 ] 本発明は、 建具、 及び建具の製造方法に関する。
背景技術
[0002] 建築物の出入口、 又は収納家具の開口に扉が用いられている。 例えば、 特 許文献 1 には、 鏡付き扉の建具が開示されている。
先行技術文献
特許文献
[0003] 特許文献 1 :実開昭 6 2 - 0 0 0 6 8 7号公報
発明の概要
発明が解決しようとする課題
[0004] ところで、 建具の芯材が木製の場合、 水分を吸収しやすく反り易くなる。
また、 芯材が金属製や樹脂製の場合、 意図しない方向からの力により反りが 生じる懸念がある。 芯材の反りは、 建具の反りの原因となる。 また、 建具に は、 搬送及び施工の負担を軽減するため、 軽量化が求められている。
[0005] 本発明は、 上記課題に鑑みてなされたものであって、 芯材の反りを緩和で き、 かつ軽量化できる建具、 及び建具の製造方法を提供することを目的とす る。
課題を解決するための手段
[0006] 第 1態様の建具は、 対向する第 1面と第 2面とを有する平板形状の芯材と 、 芯材の第 1面の側に配置された発泡体である第 1樹脂層と、 第 1樹脂層の 、 芯材とは反対側の面に配置された意匠性を有する脆性の第 1板状体とを含 む積層体、 を備える。
[0007] 第 2態様の建具は、 対向する第 1面と第 2面とを有する平板形状の芯材と 、 芯材の第 1面の側に配置された発泡体である第 1樹脂層と、 第 1樹脂層の 、 芯材とは反対側の面に配置された意匠性を有する脆性の第 1板状体と、 芯
\¥0 2020/175397 2 卩(:170? 2020 /007191
材の第 2面の側に配置された発泡体である第 2樹脂層と、 第 2樹脂層の芯材 の配置された面と反対面に配置された意匠性を有する脆性の第 2板状体とを 含む積層体、 を備える。
[0008] 第 3態様の建具の製造方法は、 対向する第 1面と第 2面とを有する平板形 状の芯材と、 芯材の前記第 1面の側に配置された発泡体である第 1樹脂層と 、 第 1樹脂層の、 芯材とは反対側の面に配置された意匠性を有する脆性の第 1板状体とを含む積層体を準備し、 芯材を切断し、 かつ第 1樹脂層の芯材の 側の _部を切断することを含む。
発明の効果
[0009] 本発明によれば、 芯材の反りを緩和でき、 かつ軽量化ができる。
図面の簡単な説明
[0010] [図 1]図 1は、 本発明による第 1実施形態の扉構造の一部を示す模式的断面図 である。
[図 2]図 2は、 本発明による第 2実施形態の扉構造の一部を示す模式的断面図 である。
[図 3]図 3は、 本発明による第 3実施形態の扉構造の斜視図である。
[図 4]図 4は図 3に示す扉構造の一部を示す模式的断面図である。
[図 5]図 5は第 3実施形態の別の形態に係る扉構造の一部を示す模式的断面図 である。
[図 6]図 6は、 本発明による扉構造の製造方法の 1実施形態の一工程を示す説 明図である。
[図 7]図 7は扉構造の製造方法の一工程を示す説明図である。
[図 8]図 8は扉構造の製造方法の一工程を示す説明図である。
[図 9]図 9は扉構造の製造方法の一工程を示す説明図である。
[図 10]図 1 0は反り量1~1。の算出するための試験方法を示す。
[図 1 1]図 1 1は反り量!· I 1の算出するための試験方法を示す。
[図 12]図 1 2は反り量!· I 1の算出するための試験方法を示す。 発明を実施するための形態
\¥0 2020/175397 3 卩(:170? 2020 /007191
[001 1 ] 以下、 添付図面にしたがって本発明の実施形態について説明する。 本発明 は以下の実施形態により説明される。 但し、 本発明の範囲を逸脱すること無 く、 多くの手法により変更を行うことができ、 本実施形態以外の他の実施形 態を利用できる。 したがって、 本発明の範囲内における全ての変更が特許請 求の範囲に含まれる。 ここで、 図中、 同 _の記号で示される部分は、 基本的 に、 同様の機能を有する同様の要素である。
[0012] <第 1実施形態>
第 1実施形態の建具を、 図面を参照して説明する。 建具として扉構造、 ホ ワイ トボード、 スクリーン、 テーブルトップ、 カウンターボードを例示する ことができる。 また、 建具として玄関収納、 クローゼッ ト、 カップボード、 テレビボード、 洗面化粧台、 トイレ、 キッチン等に用いられるパネル、 側板 、 棚板を例示することができる。 扉構造として、 内装材の扉、 玄関収納、 ク 口ーゼッ ト、 カップボード、 テレビボード、 洗面化粧台、 トイレ、 キッチン 等に用いられる鏡扉、 収納扉を例示することができる。 以下の第 1から第 3 実施形態では、 本発明を扉構造に適用した場合について説明する。 図 1は、 第 1実施形態の扉構造 1 〇を示す模式的断面図である。 図 1 に示されるよう に、 扉構造 1 〇は、 芯材 1 2と、 樹脂層 1 4と、 板状体 1 6とを含む積層体 1 7と、 を備える。
[0013] 芯材 1 2は、 対向する第 1面 1 2八と第 2面 1 2巳とを有する平板形状を 有している。 なお、 芯材 1 2の対向する 2つの主面の、 いずれを第 1面 1 2 八とし、 第 2面 1 2巳とするかは任意に決定できる。
[0014] 第 1樹脂層 1 4は発泡体である樹脂層であり、 芯材 1 2の第 1面 1 2八の側 に配置される。 板状体 1 6は意匠性を有する脆性の第 1板状体であり、 樹脂層 1 4の、 芯材 1 2とは反対側の面に配置される。 芯材 1 2と板状体 1 6とは 、 樹脂層 1 4を挟んで対向する位置に配置される。 意匠層 1 8が板状体 1 6 と樹脂層 1 4との間に配置される。
[0015] 第 1実施形態では、 板状体 1 6の意匠性は、 板状体と樹脂層との間に介在 された意匠層 1 8によって付与される。 板状体 1 6の意匠性は、 板状体自体
\¥0 2020/175397 4 卩(:17 2020 /007191
が模様や色彩等を有することで意匠性を発現してもよい。 なお、 板状体 1 6 と樹脂層 1 4との間に介在された意匠層 1 8は、 板状体 1 6の表面に直接形 成された意匠層及び樹脂層 1 4の表面に直接形成された意匠層の形態も含む
[0016] 扉構造 1 0は意匠層 1 8を備えているので、 建築物の出入口、 又は収納家 具の開口に用いられた場合、 扉構造 1 〇は高級感のある美観を演出できる。

ることが好ましい。 第 1実施形態の扉構造 1 〇の全体の厚みは、 1 0 以 上がより好ましく、 1 5
 以上がさらに好ましい。 第 1実施形態の扉構造 1 0の全体の厚みは、 2
 以下がより好ましく、 1
 以下がさらに 好ましく、
 以下が特に好ましい。
[0018] 第 1実施形態の扉構造 1 0は、 芯材 1 2の第 1面 1 2八の全体が樹脂層 1 4と板状体 1 6とにより覆われていることが好ましいが、 芯材 1 2の第 1面 1 2八の一部分が樹脂層 1 4と板状体 1 6とにより覆われていてもよい。 芯 材 1 2の第 1面 1 2 の面積のうち、 樹脂層 1 4と板状体 1 6とにより覆わ れている面積の割合は、 8 0 %以上が好ましく、 9 0 %以上がより好ましく 、 9 5 %以上がさらに好ましい。 芯材 1 2の第 1面 1 2八の面積のうち、 樹 脂層 1 4と板状体 1 6とにより覆われている面積の割合は、 1 0 0 %以下で あってもよく、 9 7 %以下であってもよい。
[0019] 第 1実施形態の扉構造 1 0の面積は、 〇. 0 1 2以上が好ましく、 0 . 1 がより好ましく、 〇. 5 2以上がさらに好ましく、 1 2以上が特に 好ましく、 2 . 5 2以上が最も好ましい。 扉構造 1 0の面積が大きいことに より反りやすく重くなるが、 樹脂層 1 4を有することにより、 反りが緩和さ れ、 軽くできる。 また、 第 1実施形態の扉構造 1 〇の面積は、 5 2以下であ ってもよく、 4 2以下であってもよく、 3 . 5 2以下であってもよく、 3 であってもよい。
[0020] 芯材 1 2の第 1面 1 2八のうち、 樹脂層 1 4と板状体 1 6とにより覆われ ている部分の面積は、 〇. 〇 1 2以上が好ましく、 〇. 1 2以上がより好
\¥02020/175397 5 卩(:170? 2020 /007191
ましく、 0. 5 m2以上がさらに好ましく、 1 m2以上が特に好ましく、 2.
5 m 2以上が最も好ましい。 また、 芯材 1 2の第 1面 1 2 Aのうち、 樹脂層 1 4と板状体 1 6とにより覆われている部分の面積は、 5 m2以下であってもよ く、 4 m2以下であってもよく、 3. 5 m2以下であってもよく、 3 m 2以下で あってもよい。
[0021] 以下、 扉構造 1 0を構成する材料について説明する。
[0022] <芯材>
芯材 1 2は、 扉構造 1 0の芯として使用される部材である。 芯材 1 2は平 板形状であり、 対向する第 1面 1 2 A及び第 2面 1 2 Bを有する。 平板形状 は、 厚みに対して面積の広い 2つの主面を有する形状である。
[0023] 芯材 1 2は、 扉構造 1 0の芯として使用される部材であるので、 剛性を有 していることが好ましい。 芯材 1 2の素材は木製であっても、 金属製であっ ても、 樹脂製であってもよく、 それらの複合体であってもよい。 扉構造 1 〇 に求められる特性に応じて、 素材を適宜選択できる。
[0024] 木製の芯材 1 2の場合、 例えば、 素材として、 中密度繊維板 (MD F (Med ium Density Fiberboard) ) 等の木質繊維板、 合板、 パーテイクルボード等 の素材を芯材 1 2として適宜用いることができる。 中密度繊維板は、 J 丨 S A 5905に規定される。 合板は、 複数の単板を積層することで構成さ れる。 パーテイクルボードは、 木材の小片を、 接着剤を使用し、 加熱圧縮す ることで製造され、 J I S A 5908に規定される。
[0025] 木製の芯材 1 2の場合、 例えば、 構造として、 木質繊維板、 合板、 パーテ イクルボード等のいわゆるソリッ ドな構造体 (ベタ芯構造) 、 及びフラッシ ュ構造板を適用できる。 フラッシュ構造板は、 木材で枠を組み、 両面に合板 等を貼り合せた中空構造であり。 ソリッ ドな構造に比較して密度を小さくで きる。
[0026] 木製の芯材 1 2の密度は、 400 k g/m3以上 900 k g/m3以下であ ることが好ましい。 芯材 1 2の密度が 400 k g /m3以上であれば、 芯材 1 2の強度を確保できる。 芯材 1 2の密度が 900 k g/m3以下であれば、 扉
\¥0 2020/175397 6 卩(:170? 2020 /007191
構造 1 〇を軽量化できる。 木製の芯材 1 2の密度は、


. 4以上〇. 9以下が好ましく、 〇. 5以上〇. 8以下がより好ましい。
[0027] 金属製の芯材 1 2の場合、 例えば、 アルミニウム、 鉄等の金属の素材を芯 材 1 2として適宜用いることができる。
樹脂製の芯材 1 2の場合、 例えば、 アクリロニトリル · ブタジエン ·スチ レン共重合合成樹脂 ( 巳 3樹脂) 、 ポリ塩化ビニル樹脂 ( 〇樹脂) 、 又はアクリル樹脂等の素材を芯材 1 2として適宜用いることができる。
[0028] 芯材 1 2の板厚は、 扉構造 1 0の厚みに応じて適宜選択される。 芯材 1 2 の板厚は、
 以下であることが好ましい。 芯材 1 2の板厚 は、 以上がより好ましく、 5 01 01以上がさらに好ましく、 1 〇111 111以 上が特に好ましい。 また、 芯材 1 2の板厚は、 2 0
 以下がより好ましく
、 以下がさらに好ましい。
[0029] <板状体>
板状体 1 6としては、 脆性材料であれば、 本発明の効果を享受できる。 脆 性とは、 力を受けた際に割れやすい性質のことを意味する。 例えば、 板状体 1 6の素材として、 ガラス板、 樹脂板やセラミック板が挙げられる。 樹脂板 は、 脆性を有する樹脂板であることが好ましい。 脆性を有する樹脂板として は、 例えば、 メラミン系樹脂板、 アクリル系樹脂板、 ポリカーボネート系樹 脂板や塩ビ板等が挙げられる。 セラミック板としては、 タイルなどの陶製の 部材が挙げられる。 板状体は石材で構成されていてもよい。 以下では、 板状 体 1 6がガラス板である場合について説明する。
[0030] 板状体 1 6に適用されるガラス板は、 ガラスの種類の点では、 特に限定さ れない。 例えば、 ソーダライムガラス、 無アルカリガラスやアルミノシリケ —トガラス等が挙げられる。 化学強化処理を施す場合には、 酸化物基準の質 量%で八 丨 2〇3を 3 %以上含有するアルミノシリケートガラスが好ましい。
[0031 ] ガラス板の板厚は、 〇. 5
 以下が好ましい。 ガラス板の板 厚が〇. 5
 以上であると、 芯材 1 2の反りを吸収できる。 ガラス板が 5
\¥0 2020/175397 7 卩(:170? 2020 /007191
以下であれば扉構造 1 0の全体が重くはならず、 搬送、 及び施工が容易 となる。 ガラス板の板厚は、 1 111 01以上がより好ましく、 1 .
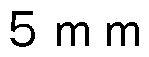 以上が さらに好ましい。 また、 ガラス板の板厚は、 4
 以下がより好ましく、 3 01 01以下がさらに好ましい。
[0032] 板状体 1 6がガラス板の場合、 ガラス板の密度は、


0 0 1< 9 / 3以下がより好ましい。 板状体 1 6の比重は、 2 . 3以上 2 . 8 以下が好ましく、 2 . 4以上 2 . 6以下が好ましい。
[0033] 板状体 1 6に適用されるガラス板は、 意匠層 1 8と密着していることが好 ましい。 密着することによって板状体 1 6を通して意匠層 1 8を見た際、 扉 構造 1 0は、 奥行き感、 高級感が増し美観上優れる。 また、 ガラス板の標準 八光源に基づく可視光透過率 (」 丨 3
 3 1 0 6に準拠して求められる
) は、 6 0 %以上であることが美観上好ましく、 より好ましくは 7 0 %以上 である。 ガラス板の標準八光源に基づく可視光透過率の上限は特に限定され ないが、 1 0 0 %以下であってもよく、 9 2 %以下であってもよく、 9 0 % 以下であってもよい。
[0034] なお、 ガラス板は、 その表面にテクスチャーを設けるために、 表面にフロ スト加工等の後加工によってテクスチャー処理を施してもよい。
[0035] ガラス板は、 公知の方法で製造できる。 すなわち、 フロート法、 フユージ ョン法、 ダウンドロー法、 口ールアウト法等によりリボン状に成形されたガ ラスを切断することにより、 ガラス板が製造される。
[0036] ガラス板は、 表層に圧縮応力層を有していてもよい。 ガラス板が強化処理 を施されると、 ガラス板は、 強化ガラス板となる。 強化処理が施された強化 ガラス板は、 強化処理が施されていない場合と比較して割れにくくなってい る。 強化ガラス板は、 表層に圧縮応力層、 すなわち、 残留圧縮応力を有する 表面層及び裏面層、 並びに表面層と裏面層との間に形成され、 残留引張応力 を有する中間層を含む。 強化ガラス板の板厚方向両端から内部に向かうほど 残留圧縮応力が小さくなり、 強化ガラス板の内部には残留引張応力が生じて
\¥0 2020/175397 8 卩(:170? 2020 /007191
いる。
[0037] 強化ガラス板の端面は、 表面層及び裏面層に連続して残留圧縮応力で覆わ れていてもよい。 強化ガラス板の端面が残留圧縮応力で覆われることで、 衝 撃に対して割れ難くなり好ましい。 なお、 強化ガラス板の端面は、 残留圧縮 応力で覆われておらず、 強化ガラス板の端面に中間層の端面が露出していて もよい。 その場合は、 樹脂などのカバー材料で覆われていることが好ましい
[0038] 強化ガラス板は、 強化処理を施すことでガラス板の表面や裏面に残留圧縮 応力を生じさせて、 作製される。 強化ガラス板は、 イオン交換法等の化学強 化処理によって得られる化学強化ガラス、 風冷強化法等の物理強化処理によ って得られる物理強化ガラスのいずれでもよい。 化学強化処理であれば、 よ り板厚の薄いガラス板であっても表面層や裏面層の残留圧縮応力の値を大き くできる。 例えば、 表層の残留圧縮応力の値は、 3 0 0 IV! 3以上が好まし く、 4 0 0 IV! 3以上がより好ましい。 表層の残留圧縮応力の上限は特に限 定されないが、 1 2 0 0 1\/1 3以下であってもよく、 8 0 0 1\/1 3以下であ ってもよく、 6 0 0 1\/1 3以下であってもよい。 化学強化ガラスの場合、 圧 縮応力層の厚みは、 5 0 以下であってもよく、 4 0 以下であっても よい。 また、 圧縮応力層の厚みは、 1 〇 以上であってもよく、 2 0 以上であってもよい。
[0039] イオン交換法は、 ガラス板の表面や裏面をイオン交換し、 ガラスに含まれ る小さなイオン半径のイオン (例えば、 !_ 丨 イオン、 N 3イオン) を大きな イオン半径のイオン (例えば、 <イオン) に置換する。 これにより、 ガラス 板の表面や裏面に残留圧縮応力を生じさせることができる。 イオン交換法で は、 ガラス板を高温の処理液に浸潰してイオン交換を行う。
[0040] 風冷強化法は、 軟化点付近の温度のガラス板を両側から急冷し、 ガラス板 の表面や裏面と、 ガラス板の内部との間に温度差をつけることで、 ガラス板 の表面や裏面に残留圧縮応力を生じさせることができる。 風冷強化法等の物 理強化法は、 強化処理に要する時間が数秒から数十秒であるため、 イオン交
\¥02020/175397 9 卩(:170? 2020 /007191
換法等による化学強化法よりも生産性が非常に優れている。
[0041] 板状体 1 6は、 樹脂層 1 4とは反対側の表面に、 特別な機能を付加するた めの機能層を有してもよい。 機能層の一例としては、 防汚膜、 抗菌膜又は防 曇膜が挙げられる。
[0042] 防汚膜は、 指紋の付着を低減させたり、 汚れを付き難く したりする効果を 有する。 特に、 扉構造 1 〇を手で直接触れると、 板状体 1 6の表面に指紋が 付着し意匠性を損なうため、 指紋の付着を低減させる A F P (A n t i -F i n g e r P r i n t ) 機能を有することが好ましい。 A F P機能は、 A F P剤を板状体 1 6に付着させて、 A F P膜をガラス板に形成する。 A F P 剤としては、 フッ素含有有機ケイ素化合物が挙げられる。 フッ素含有有機ケ イ素化合物としては、 防汚性、 撥水性及び撥油性を付与するものであれば特 に限定されず使用できる。 A F P剤の分子量は、 3, 000以上 1 0, 00 0以下が好ましく、 3, 000以上 8, 000以下がより好ましく、 3, 0 00以上 6, 000以下がさらに好ましい。 A F P剤の分子量が 3, 000 以上であることにより、 分子構造に柔軟性が付与され、 耐スクラッチ性、 表 面滑り性を得られる。 また、 1 〇, 000以下であることにより、 A F P剤 1分子あたりの反応基を十分確保でき、 板状体 1 6の表面との密着性を確保 できる。
[0043] 抗菌膜は、 抗菌性を発現させる抗菌剤を板状体 1 6に付着させて形成され る。 抗菌剤としては、 わさびをはじめとする天然抗菌剤、 銅や銀をはじめと する金属系抗菌剤、 及び酸化チタンをはじめとする酸化物系抗菌剤が挙げら れる。 特に、 銀を含有する溶液を板状体 1 6に塗布し銀膜を形成させ、 銀膜 が形成された板状体を加熱処理することにより、 板状体 1 6の表面から内部 に銀イオンを拡散させることが効果の持続性の点で好ましい。
[0044] 防曇膜は、 板状体 1 6の表面に吸水性樹脂層を設け、 板状体 1 6の板表面 に形成された微小水滴を吸水して除去することで、 板状体 1 6の表面が曇る ことを防止し、 意匠性を維持する効果を有する。 防曇膜は、 例えば、 下地層 と吸水層とを含む。 下地層は、 ガラス板から吸水層を剥がれ難くするための
\¥0 2020/175397 10 卩(:170? 2020 /007191
層であり、 例えば、 シラン系カップリング剤を含む組成物を板状体 1 6に塗 布して反応させることで得られる。 吸水層は、 硬化エポキシ樹脂、 ウレタン 樹脂及び架橋ァクリル樹脂から選ばれる硬化樹脂の原料成分を含有する組成 物を下地層上に塗布して反応させることにより得られる。
[0045] 板状体 1 6のヤング率は、 5◦ 3以上であることが好ましい。 板状体 1
6のヤング率が 5◦ 3以上であれば、 反りにくい。 板状体 1 6のヤング率 は、 1 0◦ 3以上がより好ましく、 3 0 0 9 a以上がさらに好ましく、 5 0◦ 3以上が特に好ましい。 板状体 1 6のヤング率の上限は特に限定され ないが、 1 0 0◦ 3以下であってもよい。
[0046] <意匠層>
板状体 1 6と樹脂層 1 4との間には意匠層 1 8が形成されている。 意匠層 1 8は、 例えば、 着色顔料を含む塗料を、 板状体 1 6であるガラス板の表面 に塗布して乾燥、 硬化させることによって形成される。 塗料は、 例えば、 ア クリル樹脂系塗料が挙げられる。 ァクリル樹脂系塗料は、 付着力が大きく、 耐候性、 耐食性にも優れている。 また、 仕上げが美麗である点で好ましい。 なお、 意匠層 1 8は、 意匠性を付与できるものであれば特に限定されず、 例 えば、 メラミン樹脂系塗料、 エポキシ樹脂系塗料であってもよく、 着色顔料 も様々な色であってよい。 また、 意匠層 1 8は、 金属膜をコーティングさせ た鏡であってもよい。
[0047] 塗料の塗布方法としては、 特に限定されないが、 例えば口ールコート法、 スプレーコート法、 ディップコート法、 フローコート法、 スクリーン印刷法 、 スピンコート法等が用いられる。
[0048] また、 塗料ではなく、 シート状に成形された意匠層 1 8を、 板状体 1 6で あるガラス板に接着剤などによって貼着させてもよい。 その場合、 シート状 に成形された意匠層 1 8は、 単色であっても複数色であってもよいし、 天然 石調やレンガ調等の模様が形成されていてもよい。 また、 意匠層 1 8は、 板 状体 1 6の表面に凹凸などで型模様を設けた、 例えば型板ガラスによって意 匠性を付与されていてもよい。
\¥0 2020/175397 1 1 卩(:170? 2020 /007191
[0049] <樹脂層 >
樹脂層 1 4は、 気泡 (セル) を画定する骨格樹脂を含む発泡体である樹脂 層で構成される。 発泡体である樹脂層 1 4を化学架橋法により製造する場合 、 骨格樹脂中に架橋剤を添加し、 架橋剤による架橋反応、 発泡剤の分解反応 を起こさせてガス成分を滞留させることにより、 気泡 (セル) が画定され、 所定の発泡特性を有する樹脂層 1 4を得られる。
[0050] 所定の発泡特性を得ることができれば、 骨格樹脂の種類、 及び製造方法は 限定されない。 骨格樹脂として、 合成樹脂、 合成ゴム等を使用することがで き、 例えば、 ポリェチレン、 ェチレンー酢酸ビニル共重合体 (E V A : Ethy l ene-V i ny l Acetate) 、 ェチレンープロピレンージェンゴム (E P D M) 、 シ リコーン、 ポリウレタン等を使用できる。
[0051 ] 骨格樹脂により画定される気泡は、 独立気泡体であることが好ましい。 独 立気泡体とは、 気泡がそれぞれ独立して並んでいる構造を意味する。 独立気 泡体とすることにより、 連続気泡体と比較して樹脂層 1 4の物理的強度を向 上できる。
[0052] 樹脂層 1 4の骨格樹脂は難燃剤を含んでいることが好ましい。 難燃剤によ り樹脂層 1 4の着火が抑制される。
[0053] 難燃剤として、 有機系難燃剤及び無機系難燃剤の各々を、 単独でまた混合 して骨格樹脂に加えることができる。 有機系難燃剤として、 臭素系芳香族化 合物、 例えばリン化合物等を使用できる。 また、 無機系難燃剤として、 水酸 化マグネシウム、 水酸化アルミニウム等を使用できる。 樹脂層 1 4に含まれ る難燃剤の骨格樹脂に対する質量比 (難燃剤/骨格樹脂) は、 2 0 %以上で あることが好ましく、 2 7 %以上であることがより好ましく、 3 0 %以上で あることがさらに好ましく、 5 0 %以上であることが特に好ましく、 7 0 % 以上であることが最も好ましい。 樹脂層 1 4に含まれる難燃剤の骨格樹脂に 対する質量比 (難燃剤/骨格樹脂) の上限は特に限定されないが、 1 0 0 % 以下であってもよく、 8 0 %以下であってもよく、 7 0 %以下であってもよ い。
\¥0 2020/175397 12 卩(:170? 2020 /007191
[0054] 樹脂層

層 1 4の厚みが 1
 以上であれば、 芯材 1 2の反りを吸収でき、 板状体 1 6と積層させた際に充分な耐衝撃強度が得られる。 樹脂層 1 4の厚みは、 2 111 01以上がより好ましく、 3 01〇!以上がさらに好ましい。
[0055] 樹脂層
 以下であると、 板状体 1 6の荷重による樹脂 層 1 4の変形が抑えられ、 扉構造 1 0の形状が変化しにくい。 樹脂層 1 4の 厚みは、 7
 以下がより好ましく、
 以下がさらに好ましい。
[0056] 樹脂層 1 4の密度は、
 であること が好ましい。 樹脂層
 板状体 1 6と 積層させた際に充分な耐衝撃強度が得られる。 樹脂層 1 4の密度は、 7 0 !<
 以下であ れば、 扉構造 1 0を軽量化できる。 樹脂層 1 4の密度は、 1 2 0 1< 9 /〇1 3以 下がより好ましく、 1 〇〇 1< 9 / 3以下がさらに好ましく、 8 0 1< 9 /〇^ 以下が特に好ましい。 樹脂層 1 4の比重は、 〇. 0 3以上〇. 1 6以下が好 ましい。
[0057] 樹脂層 1 4のショア八硬度は、 1 0以上、 6 0以下であることが好ましい 。 なお、 ショア八硬度は、 デュロメータ (アスカー社製アスカーゴム硬度計 八型) の測定値による。 被測定物の表面に圧子 (押針) を押し込み変形させ 、 その変形量 (押込み深さ) を測定し、 少なくとも 4か所の平均値とする。 樹脂層 1 4が薄く軟い場合には、 厚さが 6〜 1 2 になるように樹脂層を 重ね合わせて計測する。 ショア 硬度が 1 0以上であれば、 充分な剛性を有 するため施工性が良く、 また、 樹脂層 3が変形しにくいため、 板状体 1 6が 変形しにくく割れにくい。 ショア八硬度は、 より好ましくは 2 0以上であり 、 さらに好ましくは 3 0以上である。 また、 ショア八硬度が 6 0以下であれ ば、 充分な衝撃吸収性を有するため、 板状体 1 6が強い衝撃を受けたとして も割れ難い。 ショア八硬度は、 より好ましくは 5 0以下である。
[0058] 樹脂層 1 4には、 他の成分を含ませてもよい。 他の成分として、 例えば、 顔料、 無機質系添加剤等を含有できる。 樹脂層 1 4に各種機能を付与できる
\¥0 2020/175397 13 卩(:170? 2020 /007191
。 樹脂層 1 4の難燃剤等の有無は、 例えば I
 (赤外分光法) 、 丁〇 (熱 重量分析) 、 0
 (示差走査熱量分析) 等により、 測定できる。
[0059] 樹脂層 1 4は、 板形状の部材であってもよいし、 板状体 1 6に射出成型や 押出成型で一体成形されてもよい。 樹脂層 1 4が板状の部材であった場合、 意匠層 1 8が板状体 1 6と樹脂層 1 4の間に介在するように、 板状体 1 6と 板状の樹脂層 1 4とが接着剤、 粘着剤 (以下、 粘着剤を含め、 板状体用の接 着剤という。 ) 等で貼着されることが好ましい。
[0060] 板状体用の接着剤は、 樹脂層 1 4の全面に塗布されてもよいし、 一部でも よい。 接着剤を全面に塗布する方が、 板状体 1 6が割れ難くなるため有利で ある。 また、 板状体 1 6の意匠層 1 8に接着剤を塗布してもよい。 接着剤と しては、 一般的な建築用シーリング材が使用でき、 例えば変成シリコーン系 シーリング材、 アクリル系粘着剤や合成ゴム系粘着剤等が挙げられる。 接着 剤は、 両面テープのようなシート状であってもよい。 また、 接着剤は、 不燃 性が高くなるよう材料や塗布量を選定することが建築材料として好適である 板状体 1 6と板状の樹脂層 1 4との接着面積は、 板状体の面積の 1 0 %以 上が好ましく、 5 0 %以上がより好ましく、 9 0 %以上がさらに好ましく、
1 0 0 %が特に好ましい。 板状体 1 6と板状の樹脂層 1 4との接着面積の上 限は特に限定されないが、 板状体の面積の 1 0 0 %以下であってもよい。
[0061 ] 樹脂層 1 4と板状体 1 6とを一体成形させる場合は、 意匠層 1 8が形成さ れた板状体 1 6を成形型内に設置して意匠層 1 8上に樹脂が射出されて一体 成形される。 押出成型の場合は、 板状体 1 6の意匠層 1 8上に樹脂が押出型 より供給され硬化することで一体成形される。 なお、 必要に応じて、 板状体 1 6の側に接着剤や下塗り剤 (プライマー) 、 例えばシランカップリング剤 等を塗布した後に樹脂層 1 4を一体成形してもよい。
[0062] 樹脂層 1 4と芯材 1 2とは、 接着剤 (芯材用の接着剤という) を介して貼 合されることが好ましい。 芯材用の接着剤としては、 アクリル粘着系、 合成 ゴム系、 シリコーン系、 変成シリコーン系のものを使用できる。 アクリル粘
\¥0 2020/175397 14 卩(:170? 2020 /007191
着系の接着剤として、 両面テープを使用してもよい。
[0063] 第 1実施形態の扉構造 1 0は、 板状体 1 6と芯材 1 2との間に樹脂層 1 4 を有しているので、 以下の有利の点を奏する。
[0064] 芯材 1 2が、 例えば木製の場合、 水分を吸収して反りやすくなる。 芯材 1
2が、 例えば金属製の場合、 意図しない力で反りやすくなる。 しかしながら 、 扉構造 1 0の樹脂層 1 4が変形することにより、 芯材 1 2の反りを緩和で きる。 これにより、 板状体 1 6の平坦性が実現できるので、 板状体 1 6の意 匠性を確保できる。
[0065] 後述する実施例に示されるように、 芯材 1 2が単体の場合の反り量を 1~1 0と し、 積層体 1 7の反り量を!· I 1とした場合、 以下の式を満たすことができる。
[0066] ( (1~1。一1~1 1) / 1~1。) \ 1 0 0 ³ 5 %
上記式の右辺は 1 0 %が好ましく、 1 5 %がより好ましく、 2 0 %がさら に好ましい。
[0067] 樹脂層 1 4の比重は、 芯材 1 2及び板状体 1 6の比重より小さい。 扉構造
1 〇の厚みを一定とし、 芯材 1 2及び板状体 1 6のみで構成される扉構造 1 0と比較して、 芯材 1 2及び板状体 1 6の一部を樹脂層 1 4にすることで扉 構造 1 0の全体の比重を小さくできるので、 後述する実施例に示されるよう に、 扉構造 1 〇は軽量化できる。
[0068] 扉構造 1 0の比重は、 1 . 8以下が好ましい。 扉構造 1 0の比重が 1 . 8 以下であれば、 扉構造 1 〇を軽量化できる。 扉構造 1 0の比重は、 1 . 5以 下がより好ましく、 1 . 2以下がさらに好ましく、 1 . 0以下が特に好まし く、 〇. 9以下が最も好ましい。
[0069] 第 1実施形態の扉構造 1 0は、 収納家具の開口用の扉に用いることが好ま しい。
[0070] <第 2実施形態>
第 2実施形態の建具の一例を、 図面を参照して説明する。 図 2は、 第 2実 施形態の一例としての扉構造 2 0を示す模式的断面図である。 図 2に示され るように、 扉構造 2 0は、 芯材 2 2と、 第 1樹脂層 2 4と、 第 1板状体 2 6
\¥0 2020/175397 15 卩(:170? 2020 /007191
と、 第 2樹脂層 3 0と、 第 2板状体 3 2とを含む積層体 3 3と、 を備える。
[0071 ] 芯材 2 2は、 対向する第 1面 2 2 と第 2面 2 2巳とを有する平板形状を 有している。 なお、 芯材 2 2の対向する 2つの主面の、 いずれを第 1面 2 2 八とし、 第 2面 2 2巳とするかは任意に決定できる。
[0072] 第 1樹脂層 2 4は発泡体である樹脂層であり、 芯材 2 2の第 1面 2 2八の 側に配置される。 第 1板状体 2 6は意匠性を有する脆性の板状体であり、 第 1樹脂層 2 4の、 芯材 2 2と反対側の面に配置される。 芯材 2 2と第 1板状 体 2 6とは、 第 1樹脂層 2 4を挟んで対向する位置に配置される。 第 1意匠 層 2 8が第 1板状体 2 6と第 1樹脂層 2 4との間に配置される。
[0073] 第 2樹脂層 3 0は発泡体である樹脂層であり、 芯材 2 2の第 2面 2 2巳の 側に配置される。 第 2板状体 3 2は意匠性を有する脆性の板状体であり、 第 2樹脂層 3 0の、 芯材 2 2とは反対側の面に配置される。 芯材 2 2と第 2板 状体 3 2とは、 第 2樹脂層 3 0を挟んで対向する位置に配置される。 第 2意 匠層 3 4が第 2板状体 3 2と第 2樹脂層 3 0との間に配置される。
[0074] 扉構造 2 0は第 1意匠層 2 8、 及び第 2意匠層 3 4を備えるので、 建築物 の出入口に用いられた場合、 扉構造 2 0は高級感のある美観を演出できる。
[0075] 第 2実施形態の扉構造 2 0の全体の厚みは、
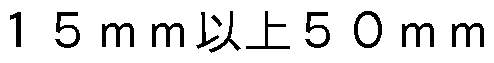 以下で あることが好ましい。 第 2実施形態の扉構造 2 0の全体の厚みは、 2 0 以上がより好ましく、 2 5
 以上がさらに好ましく、 3 0
 以上が特に 好ましい。 また、 第 2実施形態の扉構造 2 0の全体の厚みは、 4 5 以下 がより好ましく、
 以下がさらに好ましい。
[0076] 第 2実施形態の扉構造 2 0は、 芯材 2 2の第 1面 2 2八および第 2面 2 2 巳の全体が樹脂層と板状体とにより覆われていることが好ましいが、 芯材 2 2の第 1面 2 2八および第 2面 2 2巳の一部分が樹脂層と板状体とにより覆 われていてもよい。 芯材 2 2の第 1面 2 2八および第 2面 2 2巳の面積のう ち、 樹脂層と板状体とにより覆われている面積の割合は、 8 0 %以上が好ま しく、 9 0 %以上がより好ましく、 9 5 %以上がさらに好ましい。 芯材 2 2 の第 1面 2 2 および第 2面 2 2巳の面積のうち、 樹脂層と板状体とにより
\¥02020/175397 16 卩(:170? 2020 /007191
覆われている面積の割合は、 1 00%以下であってもよく、 97%以下であ ってもよい。
[0077] 第 2実施形態の扉構造 20の面積は、 〇. 01 2以上が好ましく、 0. 1 がより好ましく、 〇. 5 2以上がさらに好ましく、 1 2以上が特に 好ましく、 2. 5 2以上が最も好ましい。 扉構造 20の面積が大きいことに より反りやすく重くなるが、 樹脂層を有することにより、 反りが緩和され、 軽くできる。 また、 第 2実施形態の扉構造 20の面積は、 5 2以下であって もよく、 4 2以下であってもよく、 3. 5 2以下であってもよく、 3〇12以 下であってもよい。
[0078] 芯材 22の第 1面 22八のうち樹脂層と板状体とにより覆われている部分 の面積および芯材 22の第 2面 22巳のうち樹脂層と板状体とにより覆われ ている部分の面積は、 〇. 01 2以上が好ましく、 〇. 1 2以上がより好 ましく、 〇. 5〇12以上がさらに好ましく、 1 2以上が特に好ましく、 2.
5 2以上が最も好ましい。 また、 芯材 22の第 1面 22八のうち樹脂層と板 状体とにより覆われている部分の面積および芯材 22の第 2面 22巳のうち 樹脂層と板状体とにより覆われている部分の面積は、 5 2以下であってもよ く、 4 2以下であってもよく、 3. 5 2以下であってもよく、 3 2以下で あってもよい。
[0079] 以下、 扉構造 20を構成する材料について説明する。 なお、 第 1実施形態 と同様の構成はその説明を省略する場合がある。
[0080] <芯材>
芯材 22は、 扉構造 20の芯として使用される部材である。 芯材 22は平 板形状であり、 対向する第 1面 22 及び第 2面 22巳を有する。
[0081] 芯材 22として、 第 1実施形態の芯材 1 2と同様の素材、 及び構造を適用 できる。 第 2実施形態では、 第 1実施形態と比較して、 板厚の厚い芯材 22 が用いられることが、 積層体の剛性を増す観点から好ましい。
[0082] <板状体 >
第 1板状体 26、 及び第 2板状体 32は、 第 1実施形態の板状体 1 6と同
\¥0 2020/175397 17 卩(:170? 2020 /007191
様の板状体を適用できる。 第 2実施形態の扉構造 2 0では、 第 1板状体 2 6 と第 2板状体 3 2とは、 同じ素材又は異なる素材により構成でき、 また同じ 板厚又は異なる板厚に構成できる。
[0083] <意匠層>
第 1意匠層 2 8及び第 2意匠層 3 4は、 第 1実施形態の意匠層 1 8と同様 の意匠層を適用できる。 第 2実施形態の扉構造 2 0では、 第 1意匠層 2 8と 第 2意匠層 3 4とは、 同じ意匠層、 又は異なる意匠層で構成できる。
[0084] 扉構造 2 0の芯材 2 2の第 1面 2 2 の側と第 2面 2 2巳の側とで、 同様 の美感、 又は異なる美感を提供できる。
[0085] <樹脂層 >
第 1樹脂層 2 4及び第 2樹脂層 3 0は、 第 1実施形態の樹脂層 1 4と同様 の樹脂層を適用できる。 第 2実施形態の扉構造 2 0では、 第 1樹脂層 2 4と 第 2樹脂層 3 0とは、 同じ素材又は異なる素材で構成でき、 また同じ厚み又 は異なる厚みにできる。
[0086] 第 2実施形態の扉構造 2 0は、 第 1板状体 2 6と芯材 2 2との間に第 1樹 脂層 2 4、 及び第 2板状体 3 2と芯材 2 2との間に第 2樹脂層 3 0を有して いるので、 以下の有利の点を奏する。
[0087] 芯材 2 2が、 例えば木製の場合、 水分を吸収して反りやすくなる。 芯材 2
2が、 例えば金属製の場合、 意図しない力で反りやすくなる。 しかしながら 、 扉構造 2 0の第 1樹脂層 2 4、 及び第 2樹脂層 3 0が変形することにより 、 芯材 2 2の反りを緩和できる。 これにより、 第 1板状体 2 6、 及び第 2板 状体 3 2の平坦性が実現できるので、 第 1板状体 2 6、 及び第 2板状体 3 2 の意匠性を確保できる。
[0088] 芯材 2 2が単体の場合の反り量を 1~1 0とし、 積層体 3 3の反り量を ! ! !とし た場合、 以下の式を満たすことができる。
[0089] ( ( 1~1 0 - 1~1 1 ) / 1~1 0) \ 1 0 0 ³ 5 %
第 1樹脂層 2 4及び第 2樹脂層 3 0の比重は、 芯材 2 2、 第 1板状体 2 6 、 及び第 2板状体 3 2の比重より小さい。 扉構造 2 0の厚みを一定とし、 芯
\¥0 2020/175397 18 卩(:170? 2020 /007191
材 2 2、 第 1板状体 2 6及び第 2板状体 3 2のみで構成される扉構造 2 0と 比較して、 芯材 2 2、 第 1板状体 2 6及び第 2板状体 3 2の一部を第 1樹脂 層 2 4及び第 2樹脂層 3 0にすることで扉構造 2 0の全体の比重を小さくで きるので、 後述する実施例に示されるように、 扉構造 2 0は軽量化できる。
[0090] 扉構造 2 0の比重は、 1 . 8以下が好ましい。 扉構造 2 0の比重が 1 . 8 以下であれば、 扉構造 2 0を軽量化できる。 扉構造 2 0の比重は、 1 . 5以 下がより好ましく、 1 . 2以下がさらに好ましく、 1 . 0以下が特に好まし く、 〇. 9以下が最も好ましい。
[0091 ] 第 2実施形態の扉構造 2 0は、 建築物の出入口用の扉に用いることが好ま しい。
[0092] <第 3実施形態>
第 3実施形態の建具を、 図面を参照して説明する。 第 3実施形態の扉構造 は、 積層体の端面にモール材を備える。 第 3実施形態の扉構造は、 扉構造の 端面の強度、 及び意匠性を向上できる。
[0093] 図 3は第 3実施形態の扉構造 1 0の斜視図である。 図 3に示されるように 、 扉構造 1 0は、 芯材 1 2と、 樹脂層 1 4と、 板状体 1 6とを含む積層体 1 7と、 を備える。 積層体 1 7は、 4つの端面 1 7 を有する。 扉構造 1 0は 、 積層体 1 7の端面 1 7八を覆うモール材 6 0を備える。 図 3では、 1つの モール材 6 0のみが端面 1 7 を覆っている図が示されているが、 モール材 6 0は、 基本的には、 全ての端面 1 7 を覆う。
[0094] モール材 6 0は、 例えば、 アクリロニトリル · ブタジエン ·スチレン共重 合合成樹脂、 アクリル樹脂、 及びポリエチレンテレフタレート樹脂からなる 群より選択された材料から構成される。 モール材 6 0が積層体 1 7の端面 1 7八を覆うことにより、 モール材 6 0が端面 1 7八を保護する。 モール材 6 0は端面 1 7 に割れ、 欠け等の損傷が発生することを抑制する。
[0095] 図 4は、 図 3の扉構造 1 0の主面に直交する面で切断した端面 1 7八の一 部の模式的断面図である。 図 4に示されるように、 積層体 1 7の端面 1 7八 とモール材 6 0とは、 接着剤 6 2により結合される。 接着剤 6 2はホッ トメ
\¥0 2020/175397 19 卩(:170? 2020 /007191
ルト接着剤であることが好ましい。 ホッ トメルト接着剤は、 例えば、 特定の 温度 (1 0 0 °〇~ 2 5 0 °〇) 加熱し、 融かして使用する接着剤である。 ホッ トメルト接着剤として、 エチレン酢酸ビニル樹脂 八) 系接着剤、 ポリオレ フィン樹脂系接着剤、 及びポリウレタン樹脂 ) 系接着剤を使用できる。
[0096] 実施形態の扉構造 1 0では、 積層体 1 7の端面 1 7八が面一に構成される 。 面一とは、 積層体 1 7を構成する芯材 1 2、 樹脂層 1 4、 及び板状体 1 6 のそれぞれの端面の間の段差が、 ± 0 . 5
 以内の範囲にあることを意味 する。 積層体 1 7の端面 1 7八が面一であるので、 接着剤 6 2を均一の厚み で形成できる。 このため、 端面 1 7八とモール材 6 0との接着強度を向上で きる。
[0097] 実施形態の扉構造 1 0では、 積層体 1 7が樹脂層 1 4を有するので、 樹脂 層を備えない単体の板状体と比較して、 板状体 1 6の厚みを薄くできる。 板 状体 1 6が透明な厚みの薄いガラス板の場合、 人が板状体 1 6の端面から接 着剤 6 2を視認できにくくなる。 接着剤 6 2が視認されないことで、 扉構造 1 0の意匠性が向上できる。
[0098] また、 実施形態の扉構造 1 0では、 積層体 1 7が樹脂層 1 4を有するので 、 樹脂層を備えない単体の板状体と比較して、 積層体 1 7の端面 1 1 !\ヒモ —ル材 6 0との接着強度を向上できる。 接着剤 6 2と樹脂層 1 4との接着強 度が、 接着剤 6 2と板状体 1 6との強度より大きい。 したがって、 樹脂層を 備えない単体の板状体と比較して、 樹脂層 1 4が存在することで、 接着剤 6 2によりモール材 6 0と樹脂層 1 4とが強固に接着できる。
[0099] 図 5は第 3実施形態の別の形態に係る扉構造 2 0の一部の模式的断面図で ある。 扉構造 2 0は、 芯材 2 2と、 第 1樹脂層 2 4と、 第 1板状体 2 6と、 第 2樹脂層 3 0と、 第 2板状体 3 2とを含む積層体 3 3と、 を備える。 積層 体 3 3の端面 3 3八とモール材 6 0とが接着剤 6 2により結合される。 第 3 実施形態の別の形態に係る扉構造 2 0は、 第 3実施形態の扉構造 1 0と同様 の効果を奏する。
[0100] <建具の製造方法>
\¥0 2020/175397 20 卩(:170? 2020 /007191
次に、 図 6から図 9を参照して、 本発明による建具の製造方法の 1実施形 態を説明する。 この実施形態に係る建具の製造方法は、 第 1実施形態、 及び 第 3実施形態の扉構造 1 0を参照して説明する。
[0101 ] 図 6に示されるように、 芯材 1 2と、 第 1樹脂層 1 4と、 第 1板状体 1 6 とが準備される。 樹脂層 1 4と板状体 1 6とは、 ほぼ同じ面積を有している 。 したがって、 樹脂層 1 4の端面と板状体 1 6の端面とは面一となる。 ここ で面積は、 樹脂層 1 4の主面、 及び板状体 1 6の主面の面積である。
[0102] 一方、 芯材 1 2の面積は、 樹脂層 1 4及び板状体 1 6の面積より大きい。
したがって、 芯材 1 2は、 樹脂層 1 4及び板状体 1 6から突出する。 積層体 1 7の端面 1 7八は面一に構成されていない。
[0103] 次に、 図 7に示されるように、 切断刃 7 0が、 板状体 1 6の端面に沿って 、 芯材 1 2と樹脂層 1 4の一部とを切断する。 切断刃 7 0は、 芯材 1 2を完 全に切断する。 一方、 切断刃 7 0は、 樹脂層 1 4の一部を切断し、 板状体 1 6の側から距離八の樹脂層 1 4を残す。 したがって、 切断刃 7 0は板状体 1 6に接触しないため、 切断刃 7 0に起因する損傷から板状体 1 6を保護する ことが可能となる。
[0104] 次に、 図 8に示されるように、 切断された芯材 1 2の突出部が取り除かれ 、 積層体 1 7の端面 1 7八が面一となる。 積層体 1 7の端面 1 7八が面一で ある扉構造 1 0が製造される。
[0105] 実施形態と異なり、 樹脂層を備えない単体の板状体と芯材とから構成され る積層体では、 芯材のみを切断することは困難である。 板状体と、 板状体の 面積より大きい芯材とから構成される積層体を準備し、 板状体の端面に沿っ て切断刃で切断する場合、 次の懸念がある。 芯材を完全に切断する場合、 切 断刃が板状体と接触し、 板状体に損傷を与えやすく、 板状体が割れやすい。 一方、 板状体と接触しないように芯材に切断刃を挿入しても、 芯材が切断さ れず、 板状体からの芯材の突出部を取り除くことが難しい。 芯材に無理に力 を掛けて突出部を取り除くと、 積層体の端面が面一とならない懸念がある。 実施形態では積層体 1 7が樹脂層 1 4を含んでいるので、 上記懸念を解消で
\¥0 2020/175397 21 卩(:170? 2020 /007191
きる。
[0106] 次に、 図 9に示されるように、 扉構造 1 0の積層体 1 7の端面 1 7八に、 モール材 6 0が取り付けられる。 モール材 6 0は、 例えば、 縁貼り機 (エッ ジバンダー) により、 積層体 1 7の端面 1 7八に取り付けられ、 図 3に示さ れる扉構造 1 0が製造される。
[0107] 縁貼機 (不図示) は、 例えば、 扉構造 1 0を搬送する搬送ユニッ トと、 端 面 1 7 にホッ トメルト接着剤を塗布する塗布ユニッ トと、 モール材 6 0を 取り付ける押し付けユニッ トと等を備える。 扉構造 1 〇は、 搬送ユニッ トに 搬送されながら、 塗布ユニッ トにより端面 1 7 に接着剤が塗布され、 次い で押し付けユニッ トによりモール材 6 0が端面 1 7八に取り付けられる。 こ のようにして、 積層体 1 7の 1つの端面 1 7八にモール材 6 0が取り付けら れる。 残りの 3つ端面 1 7八にも、 同様にしてモール材 6 0が取り付けられ る。
[0108] 実施形態の積層体 1 7は、 切断刃 7 0により端面 1 7八が面一とされる。
したがって、 縁貼機を用いたモール材 6 0の取り付けが可能となる。
[0109] 実施形態と異なり、 樹脂層を備えない単体の板状体と芯材とから構成され 積層体では、 上述したように端面を面一することができないため、 縁貼機を 用いたモール材の取り付けが困難であった。 実施形態の扉構造 1 0は、 縁貼 機の使用を可能にする。
[01 10] <実施例>
以下の扉構造の実施例により本発明を具体的に説明するが、 本発明の建具 はこれらの実施例によって限定されるものではない。
[01 1 1 ] (試験 1)
第 1実施形態の扉構造について、 芯材の反りの緩和を確認するため、 反り 吸収性試験を行った。
[01 12] (試験体)
試験体として、 平面視で 4 0 0 01 01の短辺と、 1 0 0 0 111 111の長辺とを有 する矩形形状の扉構造であって、 (1) 5 . 5
 の芯材と 2 のガラス
\¥02020/175397 22 卩(:170? 2020 /007191
板、 (2) 5. 5〇!〇!の芯材と 2〇!〇!の樹脂層と 2〇!〇!のガラス板、 (3)
5. 5〇!〇!の芯材と 3〇!〇!の樹脂層と 2〇!〇!のガラス板、 (4) 5. 5111111 の芯材と 4〇!〇!の樹脂層と 2〇!〇!のガラス板、 (5) 5. 5111111の芯材と 5
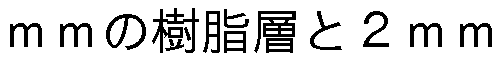 のガラス板、 の 5種類の扉構造を準備した。 芯材とし て木製の芯材 (IV! 0 ) を使用した。 また、 樹脂層として 65 (1^ 9/0^) の見かけ密度、 及び 65 (k P a) の 25%圧縮応力を有する樹脂層を使用 した。 板状体として、 ソーダライムガラス (八〇〇社製: 1_ 2) を使用し た。
[0113] (試験方法)
反り量 |~|0が異なる 3種類の芯材を模擬するために、 図 1 0に示されるよう に、 平坦な芯材 1 2を平坦面 50の上に載置し、 芯材 1 2の長辺の中心部と 、 平坦面 50の間に、 短辺に平行なスぺーサ 52を揷入した。
[0114] 芯材 1 2の反り量 1~10は、 スぺーサ 52を揷入する前の平坦な芯材 1 2を基 準面とし、 その基準面からスぺーサ 52を揷入した後の反った芯材 1 2の頂 部までの距離を測定することにより求めた。
[0115] スぺーサ 52の厚みを変えることにより、 芯材 1 2の複数の反り量 1~10を算 出した。
[0116] 図 1 1 に示される方法で、 (1) の構造の積層体の反り量 !!!を算出した。
図 1 1 に示されるように、 芯材 1 2とガラス板◦とを有する積層体 31 を芯 材 1 2の側を平坦面 50に載置して、 積層体 31の長辺の中心部と、 平坦面 50の間に、 短辺に平行なスぺーサ 52を揷入した。 図 1 1では、 スぺーサ 52として、 図 1 0において芯材 1 2の反り量 1~1。を算出する際に利用した複 数のスぺーサ 52を利用した。
[0117] 積層体 31の反り量!· I 1は、 スぺーサ 52を揷入する前の平坦な積層体 31 のガラス板を基準面とし、 その基準面からスぺーサ 52を揷入した後の反っ た積層体 31の頂部までの距離を測定することにより求めた。
[0118] 図 1 2に示される方法で、 (2) 〜 (5) の構造の積層体の反り量 !!!を算 出した。 図 1 2に示されるように、 芯材 1 2と樹脂層 1 4とガラス板◦とを
\¥0 2020/175397 23 卩(:170? 2020 /007191
有する積層体 3 2を芯材 1 2の側を平坦面 5 0に載置して、 積層体 3 2の長 辺の中心部と、 平坦面 5 0の間に、 短辺に平行なスぺーサ 5 2を揷入した。 図 1 2では、 スぺーサ 5 2として、 図 1 0において芯材 1 2の反り量1~1。を算 出する際に利用した複数のスぺーサ 5 2を利用した。 積層体 3 2の反り量 1~1 ! は、 スぺーサ 5 2を揷入する前の平坦な積層体 3 2のガラス板を基準面とし 、 その基準面からスぺーサ 5 2を揷入した後の反った積層体 3 2の頂部まで の距離を測定することにより求めた。 図 1 2に示される積層体が実施形態の 積層体を構成する。
[01 19] (試験結果)
芯材 1 2の反り量 1~1。に対する、 5種類の積層体の試験体の反り量 ! ! !を求 め、 以下の式により吸収率 (%) を求めた。
[0120] ( 〇- ) / ! !〇) X 1 0 0 (%)
表 1は扉構造と反り量!· I。、反り量 ! ! !、 吸収率、 せん断応力、 及び応力緩和 率の結果を記載した表である。
[0121 ] [表 1 ]

[0122] 例 1、 例 6、 及び例 1 1は樹脂層 1 4を備えていない。 その結果、 吸収率 は 5 %未満である。
[0123] 樹脂層 1 4を備える例 2〜例 5、 例 7〜例 1 0、 及び例 1 2〜 1 5は、 5 (%) 以上の吸収率を達成できる。 また、 樹脂層 1 4の厚みが大きくなる程
\¥0 2020/175397 24 卩(:170? 2020 /007191
、 吸収率が大きくなることが理解できる。
[0124] また、 扉構造のガラス板の接着界面に発生するせん断応力の最大値 、 反 り量 1~1 0の芯材にガラス板単体を接着したときのガラス板に発生するせん断応 力の最大値 0、 および応力緩和率を表 1 に示す。 ガラス板の接着界面に発生 するせん断応力は、 (1\/1 ) / (2 X 1) であり、 IV!は曲げモーメント、
IIはガラス板の厚み、 丨 は断面 2次モーメントである。 応力緩和率は以下の 式により求められる。
( <70—(7〗) /(70X 1 0 0
樹脂層 1 4を備える例 2〜例 5、 例 7〜例 1 0、 及び例 1 2〜 1 5は、 5 (%) 以上の応力緩和率を達成できる。 また、 樹脂層 1 4の厚みが大きくな る程、 応力緩和率が大きくなることが理解できる。 例 2〜例 5、 例 7〜例 1 0、 及び例 1 2〜 1 5の扉構造は、 樹脂層 1 4を備えるため、 ガラス板の接 着界面に発生するせん断応力が小さく、 ガラス板と芯材とが剥離しにくい。
[0125] (試験 2)
第 1実施形態の扉構造について、 比重を算出した。 芯材として IV! 0 (比 重: 0 . 8) 又はフラッシュ構造板 (比重: 0 . 5) 、 樹脂層としてポリエ チレン (比重: 〇. 0 7)
、 及び板状体としてガラス板 (比重: 2 . 5) を組み合わせて扉構造とした
[0126] 表 2は IV! 0 を芯材とした場合の比重を算出した表であり、 表 3はフラッ シュ構造板を芯材とした場合の比重を算出した表である。 比重は以下の式で 求めた。
[0127] 複合体比重 =
 / ( ^ + I 2 + I
3)
(但し、 ¢1 1 :板状体の比重、
 2 :樹脂層の比重、 ¢1 3 :芯材の比重、 1 :板状体の厚み、 1 2 :樹脂層の厚み、 1 3 :芯材の厚み)
例 1 6〜例 2 0
 は、 芯材の厚みを
 樹脂層の厚みと ガラス板の厚みとを変更した扉構造を示す。 なお、 実施例において、 樹脂層
\¥0 2020/175397 25 卩(:170? 2020 /007191
の厚み 0 . 0 (111 111) 、 及びガラス板の厚み 0 . 0 (01 01) は、 それらを備 えていないことを意味する。
[0128] 例 2 1〜例 2 5 (〇[¾ 2) は、 総厚みを 1 7 とし、 樹脂層の厚みとガ ラス板の厚みとを変更した扉構造を示す。 例 2 6〜例 3 0 (〇[¾ 3) は、 総 厚みを 2 0 とし、 樹脂層の厚みとガラス板の厚みとを変更した扉構造を す。
[0129] [表 2]

[0130] 表 2の結果から、 芯材とガラス板とで構成される扉構造である例 2 0、 例
2 5、 及び例 3 0は、 各グループ の中で、 比重が最も大 きかった。 芯材のみの例 1 6、 例 2 1、 及び例 2 6は、 各グループ (◦[¾ 1 の中で、 比重は下から 2番目であった。 しかしながら、 表 1の結 果に示されるように反り量は緩和されない。
[0131 ] 実施例である例 1 7〜例 1 9、 例 2 2〜例 2 4、 例 2 7〜例 2 9において 、 1 の樹脂層と 5 のガラス板の組み合わせの扉構造である例 1 8、 例 2 3、 及び例 2 8の比重が、 各グループ
 の実施例の中 で、 最も大きかった。 1 0 111 111の樹脂層と〇. 5〇!〇!のガラス板で構成され
\¥0 2020/175397 26 卩(:170? 2020 /007191
る実施形態の扉構造の例 1 9、 例 2 4、 及び例 2 9の比重が各グループ (◦ の実施例の中で、 最も小さかった。 実施例の扉構造 (例 1 7 〜例 1 9、 例 2 2〜例 2 4、 例 2 7〜例 2 9) は 1 . 8以下の比重であった
[0132] 例 3 1〜例 3 5は、 芯材の厚みを とし、 樹脂層の厚みとガラス板の 厚みとを変更した扉構造を示す。 例 3 6〜例 4 0は、 総厚みを 1 7 とし 、 樹脂層の厚みとガラス板の厚みとを変更した扉構造を示す。 例 4 1〜例 4 5は、 総厚みを 2 0 01 111とし、 樹脂層の厚みとガラス板の厚みとを変更した 扉構造を示す。
[0133] [表 3]

[0134] 表 3の結果から、 芯材とガラス板とで構成される扉構造である例 3 5、 例 4 0、 及び例 4 5は、 各グループ の中で、 比重が最も大 きかった。 芯材のみの例 3 1、 例 3 6、 及び例 4 1は、 各グループ
の中で、 比重は下から 2番目であった。 しかしながら、 表 1の結 果に示されるように反り量は緩和されない。
\¥0 2020/175397 27 卩(:170? 2020 /007191
[0135] 実施例である例 3 2〜例 3 4、 例 3 7〜例 3 9、 例 4 2〜例 4 4において 、 1 の樹脂層と
 のガラス板の組み合わせの扉構造である例 3 3、 例 3 8、 及び例 4 3の比重が、 各グループ
 の実施例の中 で、 最も大きかった。 1 0 111 111の樹脂層と〇. 5〇!〇!のガラス板で構成され る実施形態の扉構造の例 3 4、 例 3 9、 及び例 4 4の比重が各グループ (◦
 の実施例の中で、 最も小さかった。 実施例の扉構造 (例 3 2 〜例 3 4、 例 3 7〜例 3 9、 例 4 2〜例 4 4) は 1 . 8以下の比重であった
[0136] (試験 3)
第 2実施形態の扉構造について、 比重を算出した。 芯材として 1\/1 0 (比 重: 0 . 8) 又はフラッシュ構造板 (比重: 0 . 5) 、 樹脂層としてポリエ チレン (比重: 〇. 0 7) 、 及び板状体としてガラス板 (比重: 2 . 5) を 組み合わせて扉構造とした。
[0137] 表 4は IV! 0 を芯材とした場合の比重を算出した表であり、 表 5はフラッ シュ構造板を芯材とした場合の比重を算出した表である。
[0138] 例 4 6〜例 5 0
 は、 総厚みを
 樹脂層の厚みとガ ラス板の厚みとを変更した扉構造を示す。 第 2実施形態の扉構造は、 芯材を 挟んで 2つの樹脂層と、 2つのガラス板と、 を備えている。 表 4中の樹脂層 の厚みは 2つ樹脂層の合計厚みであり、 ガラス板の厚みは 2つのガラス板の 合計厚みを示す。
[0139] [表 4]

[0140] 表 4の結果から、 芯材とガラス板とで構成される扉構造である例 5 0は、
\¥0 2020/175397 28 卩(:170? 2020 /007191
グループ〇[¾ 7の中で、 比重が最も大きかった。 芯材のみの例 4 6は、 グル
 の中で、 比重は下から 2番目であった。 しかしながら、 表 1の結 果に示されるように反り量は緩和されない。
[0141] 実施例である例 4 7〜例 4 9において、 2
 の樹脂層と 1
 のガラ ス板の組み合わせの扉構造である例 4 8の比重が、 グループ〇
 7の実施例 の中で、 最も大きかった。 2 0 111 111の樹脂層と 1 . 0
 のガラス板で構成 される実施形態の扉構造の例 4 9の比重がグループ〇
 7で、 最も小さかっ た。 実施例の扉構造 (例 4 7〜例 4 9) は 1 . 8以下の比重であった。
[0142] 例 5 1〜例 5 5 (〇[¾ 8) は、 総厚みを
 樹脂層の厚みとガ ラス板の厚みとを変更した扉構造を示す。 表 5中の樹脂層の厚みは 2つ樹脂 層の合計厚みであり、 ガラス板の厚みは 2つのガラス板の合計厚みを示す。
[0143] [表 5]

[0144] 表 5の結果から、 芯材とガラス板とで構成される扉構造である例 5 5は、 グループ〇[¾ 8の中で、 比重が最も大きかった。 芯材のみの例 5 1は、 グル
 の中で、 比重は下から 2番目であった。 しかしながら、 表 1の結 果に示されるように反り量は緩和されない。
[0145] 実施例である例 4 7〜例 4 9において、 2
 の樹脂層と 1
 のガラ ス板の組み合わせの扉構造である例 5 3の比重が、 グループ〇
 7の実施例 の中で、 最も大きかった。 2 0 111 111の樹脂層と 1 . 0
 のガラス板で構成 される実施形態の扉構造の例 5 4の比重がグループ〇 8で、 最も小さかっ た。 実施例の扉構造 (例 4 7〜例 4 9) は 1 . 8以下の比重であった。 符号の説明
\¥02020/175397 29 卩(:170? 2020 /007191
[0146] 1 0 扉構造、 1 2 芯材、 1 2八 第 1面、 1 2巳 第 2面、 1 4 樹脂 層、 1 6 板状体、 1 8 意匠層、 20 扉構造、 22 芯材、 22八 第 1面、 226 第 2面、 24 第 1樹脂層、 26 第 1板状体、 28 第 1 意匠層、 30 第 2樹脂層、 32 第 2板状体、 34 第 2意匠層、 50 平坦面、 52 スぺーサ、 60 モール材、 62 接着剤◦ ガラス板、 3 1 積層体、 32 積層体
201 9年 2月 28日に出願された日本国特願 201 9-035638号 及び 201 9年 1 0月 1日に出願された日本国特願 201 9— 1 81 244号 の明細書、 特許請求の範囲、 図面及び要約書の全内容をここに引用し、 本発 明の明細書の開示として、 取り入れるものである。
Claims
[請求項 1 ] 対向する第 1面と第 2面とを有する平板形状の芯材と、
前記芯材の前記第 1面の側に配置された発泡体である第 1樹脂層と 前記第 1樹脂層の、 前記芯材とは反対側の面に配置された意匠性を 有する脆性の第 1板状体とを含む積層体、 を備える建具。
[請求項 2] 前記芯材の前記第 2面の側に配置された発泡体である第 2樹脂層と 前記第 2樹脂層の、 前記芯材とは反対側の面に配置された意匠性を 有する脆性の第 2板状体とをさらに含む積層体、 を備える請求項 1 に 記載の建具。
[請求項 3] 前記第 1樹脂層が独立気泡体である、 請求項 1又は 2に記載の建具
[請求項 4] 前記第 2樹脂層が独立気泡体である、 請求項 2に記載の建具。
[請求項 5] 前記芯材が木製の芯材である、 請求項 1から 4のいずれか一項に記 載の建具。
[請求項 6] 前記木製の芯材が中密度繊維板、 フラッシュ構造板、 又はパーティ クルボードである請求項 1から 5のいずれか一項に記載の建具。
[請求項 7] 前記芯材が金属製または樹脂製の芯材である、 請求項 1から 6のい ずれか一項に記載の建具。
[請求項 8] 前記芯材が単体の場合の反り量を 1~1 0とし、 前記積層体の反り量を
1~1 1とした場合、
( (H〇- H 1) / ! !〇) X I 0 0 ³ 5 %を満たす、
請求項 1から 7のいずれか一項に記載の建具。
[請求項 9] 前記建具の比重が 1 . 8以下である、 請求項 1から 8のいずれか一 項に記載の建具。
[請求項 10] 前記第 1板状体、 及び前記第 2板状体がガラス板である請求項 1か ら 9のいずれか一項に記載の建具。
\¥0 2020/175397 31 卩(:170? 2020 /007191
[請求項 1 1 ] 前記芯材が2 01 01以上の厚みを有し、 前記第

1 0 111〇!の厚みを有し、 前記第 1板状体が〇.

みを有する請求項 1から 1 〇のいずれか一項に記載の建具。
[請求項 12] 前記第 2樹脂層が 1 01 01から 1 0 01 01の厚みを有し、 第 2板状体が 〇. 5〇!〇!から 5〇!〇!の厚みを有する請求項 1 1 に記載の建具。
[請求項 13] 前記積層体の端面を覆うモール材を備える請求項 1から 1 2のいず れか一項に記載の建具。
[請求項 14] 前記積層体の端面が面一である請求項 1 3に記載の建具。
[請求項 15] 前記モール材がアクリロニトリル · ブタジエン ·スチレン共重合合 成樹脂、 アクリル樹脂、 及びポリエチレンテレフタレート樹脂からな る群より選択された材料から構成される請求項 1 3又は 1 4に記載の 建具。
[請求項 16] 前記建具は扉構造である、 請求項 1から 1 5のいずれか一項に記載 の建具。
[請求項 17] 対向する第 1面と第 2面とを有する平板形状の芯材と、 前記芯材の 前記第 1面の側に配置された発泡体である第 1樹脂層と、 前記第 1樹 脂層の、 前記芯材とは反対側の面に配置された意匠性を有する脆性の 板状体とを含む積層体を準備し、
前記芯材を切断し、 かつ前記第 1樹脂層の前記芯材の側の一部を切 断することを含む建具の製造方法。
[請求項 18] 前記芯材と前記第 1樹脂層とが前記第 1板状体より大きな面積を有 し、
前記第 1板状体の端面に沿って、 前記芯材、 及び前記第 1樹脂層の 一部を切断し、 前記積層体の端面を面一にすることを含む請求項 1 7 に記載の建具の製造方法。
[請求項 19] 前記積層体の端面にモール材を取り付けることを含む請求項 1 8に 記載の建具の製造方法。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2021502216A JP7362043B2 (ja) | 2019-02-28 | 2020-02-21 | 建具、及び建具の製造方法 |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2019035638 | 2019-02-28 | ||
| JP2019-035638 | 2019-02-28 | ||
| JP2019-181244 | 2019-10-01 | ||
| JP2019181244 | 2019-10-01 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2020175397A1 true WO2020175397A1 (ja) | 2020-09-03 |
Family
ID=72239945
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2020/007191 Ceased WO2020175397A1 (ja) | 2019-02-28 | 2020-02-21 | 建具、及び建具の製造方法 |
Country Status (2)
| Country | Link |
|---|---|
| JP (1) | JP7362043B2 (ja) |
| WO (1) | WO2020175397A1 (ja) |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS488030U (ja) * | 1971-06-08 | 1973-01-29 | ||
| JP2001227251A (ja) * | 2000-02-17 | 2001-08-24 | Aica Kogyo Co Ltd | ド ア |
| JP2003171629A (ja) * | 2001-12-03 | 2003-06-20 | Miyata Ind Co Ltd | 自転車用チューブラータイヤの接着用粘着両面テープおよびチューブラーリムへの接着方法 |
| JP2006316512A (ja) * | 2005-05-13 | 2006-11-24 | Yamanaka Sangyo Kk | 建具構成芯材および建具構成芯材を用いた襖 |
| JP2015028251A (ja) * | 2013-07-30 | 2015-02-12 | パナソニック株式会社 | 建具 |
| JP2016125227A (ja) * | 2014-12-26 | 2016-07-11 | 永大産業株式会社 | 建具及び建具の製造方法 |
| JP2017105158A (ja) * | 2015-11-30 | 2017-06-15 | パナソニックIpマネジメント株式会社 | 化粧パネル及びパネル製造方法 |
| US20180087315A1 (en) * | 2016-09-27 | 2018-03-29 | Aadg, Inc. | Polycarbonate honeycomb core door and method of making same |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2006316521A (ja) | 2005-05-13 | 2006-11-24 | Unit Safety Sign Co Ltd | 反射チェーン |
-
2020
- 2020-02-21 JP JP2021502216A patent/JP7362043B2/ja active Active
- 2020-02-21 WO PCT/JP2020/007191 patent/WO2020175397A1/ja not_active Ceased
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS488030U (ja) * | 1971-06-08 | 1973-01-29 | ||
| JP2001227251A (ja) * | 2000-02-17 | 2001-08-24 | Aica Kogyo Co Ltd | ド ア |
| JP2003171629A (ja) * | 2001-12-03 | 2003-06-20 | Miyata Ind Co Ltd | 自転車用チューブラータイヤの接着用粘着両面テープおよびチューブラーリムへの接着方法 |
| JP2006316512A (ja) * | 2005-05-13 | 2006-11-24 | Yamanaka Sangyo Kk | 建具構成芯材および建具構成芯材を用いた襖 |
| JP2015028251A (ja) * | 2013-07-30 | 2015-02-12 | パナソニック株式会社 | 建具 |
| JP2016125227A (ja) * | 2014-12-26 | 2016-07-11 | 永大産業株式会社 | 建具及び建具の製造方法 |
| JP2017105158A (ja) * | 2015-11-30 | 2017-06-15 | パナソニックIpマネジメント株式会社 | 化粧パネル及びパネル製造方法 |
| US20180087315A1 (en) * | 2016-09-27 | 2018-03-29 | Aadg, Inc. | Polycarbonate honeycomb core door and method of making same |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7362043B2 (ja) | 2023-10-17 |
| JPWO2020175397A1 (ja) | 2020-09-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US9339993B2 (en) | Appliance fascia and mounting therefore | |
| EP3030529B1 (en) | Polymer edge-covered glass articles and methods for making and using same | |
| US20200262184A1 (en) | Asymmetric glass laminates | |
| CN108290388A (zh) | 具有强化的衰减性质的层叠体结构 | |
| US20190054717A1 (en) | Asymmetric glass laminates exhibiting improved damage tolerance | |
| EP3463864B1 (en) | Laminated glass structures with enhanced thermal and moisture-resistance | |
| TW202110756A (zh) | 具有降低的彎曲應力和改善的hit性能的汽車內飾的層壓方法 | |
| JPWO2017090679A1 (ja) | 扉体 | |
| JP6614235B2 (ja) | 化粧板 | |
| JP7362043B2 (ja) | 建具、及び建具の製造方法 | |
| JP7410454B2 (ja) | 建具、及び建具の製造方法 | |
| US11247435B2 (en) | Glass laminates with improved flatness and methods for forming the same | |
| US10479051B2 (en) | Decorative panel | |
| JP7655222B2 (ja) | 化粧材及び該表面保護層形成用樹脂組成物 | |
| KR20210122973A (ko) | Pvc 시트로 마감하여 내오염성과 내충격성이 우수한 기능성 목재문 | |
| JP7288584B2 (ja) | 建具 | |
| KR101299156B1 (ko) | 내구성 및 가공성이 우수한 화장실용 칸막이 및 그 제조 방법 | |
| JP7037746B2 (ja) | 化粧板 | |
| KR20100027611A (ko) | 클릭 합판마루 | |
| CN109562605B (zh) | 装饰板 | |
| KR102258136B1 (ko) | 재단품질이 개선된 인테리어용 패널 | |
| KR101231651B1 (ko) | 고강도 내취성 기재가 접착된 유리 인테리어 장식재 | |
| NL2013100B1 (en) | Panel suitable for installation of a waterproof floor or wall covering, method of producing a panel. | |
| KR20240100958A (ko) | 가구용 패널 | |
| CN205044245U (zh) | 一种带人造皮革和复合有板材的玻璃 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 20763286 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2021502216 Country of ref document: JP Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 20763286 Country of ref document: EP Kind code of ref document: A1 |