US1854872A - Manufacture of sheets or slabs - Google Patents
Manufacture of sheets or slabs Download PDFInfo
- Publication number
- US1854872A US1854872A US246345A US24634528A US1854872A US 1854872 A US1854872 A US 1854872A US 246345 A US246345 A US 246345A US 24634528 A US24634528 A US 24634528A US 1854872 A US1854872 A US 1854872A
- Authority
- US
- United States
- Prior art keywords
- oven
- sheets
- sheet
- machine
- manufacture
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B1/00—Producing shaped prefabricated articles from the material
- B28B1/52—Producing shaped prefabricated articles from the material specially adapted for producing articles from mixtures containing fibres, e.g. asbestos cement
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B11/00—Apparatus or processes for treating or working the shaped or preshaped articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B11/00—Apparatus or processes for treating or working the shaped or preshaped articles
- B28B11/24—Apparatus or processes for treating or working the shaped or preshaped articles for curing, setting or hardening
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B19/00—Machines or methods for applying the material to surfaces to form a permanent layer thereon
- B28B19/0092—Machines or methods for applying the material to surfaces to form a permanent layer thereon to webs, sheets or the like, e.g. of paper, cardboard
Definitions
- UPSON OI LOCKPORT, NEW YORK, ASSIGNOR TO THE UPSON COMPANY,
- My present invention relates to the manufacture of sheets or slabs, particularly when composed in whole or in part of material originally in the plastic state, and it has for its object an improved process or method, and a simple compact and efficient machine for producing a product of this kind.
- a further object of the invention is to produce in an economical manner a high grade of wallboard for building constructions, and similar sheets, my invention contemplating their production as a continuous forming operation.
- the improvements are directed in part toward the provision of means for preliminarily hardening the product after it issues from the forming element, so that it can be safely and conveniently manipulated without injury in passing it to a drying and curing medium.
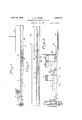
- Fig. 1 is a side view of the feed and forming end of the machine broken away, and showing one embodiment of my invention
- Fig. 2 is a side view of the intermediate portion of the machine broken away at both ends and forming a continuation of Fig. 1;
- Fig. 3 is a side View of the delivery end of the machine broken away at one end, and forming a continuation of Fig. 2;
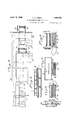
- Fig. 4 is a top view broken away of the portions of the machine shown in Figs. 1, 2 and 3, but condensed;
- Fig. 5 is an enlarged fragmentary sectional view of a portion of the platen bed with a fragment of the product in formation therebetween;
- Fig.6 is an enlarged section on the line 66 of Fig. 4;
- Fig. 7 is an enlarged section on the line 77 of Fig 4;
- Fig. 8 is an enlarged section on the line 8-8 of Fig. 4;
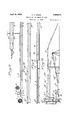
- Fig. 9 is a side view of the feed and forming end of a modified embodiment of tion broken away;
- Fig. 10 is a broken side view of an intermediate continuation of the oven shown at the top of Fig. 9, the two views being connected B to B;
- Fig. 11 is a broken side view of the intermediate portion of the lower platen section of Fig. 9, being connected A to A to the last mentioned figure and Fig. 12 is a broken continuation of both Figs. 10 and 11 continued B to B and A to A, and showing the delivery end of the machine.
- the -present machine and method in the two embodiments shown has been specially designed for the manufacture of a special wallboard, preferably composed of two outer paper facings, or liners, as they are called, and a cellular fire-resisting and insulating mineral bod of substantial thickness therebetween.
- a mixture having as the principal ingredients sodium silicate and a filler of finely comminuted or powdered dolomitic limestone provides a suitable body between the paper walls for the purposes of producing such a 1product.
- Such a mixture is intumescent in c aracter, and puffs up into a cellular or s onge-like consistency when confined and subjected to a proper de cc of heat. It can later be hardened an dried and assumes a solid texture, in which state it is hard and relatively stiff without being brittle.
- My invention contemplates producing such a board continuously in a moving strip or sheet that is finally cut-into lengths.
- I provide a supply of paper consisting of two strips which are brought together one upon another and a suitable amount of theplastic material fed between them. This laminated the invenmass is passed between a air of upper and lower heated platens which presents smooth walls of considerable extent and whose separation regulates the thickness of the product. These platens are heated by steam or otherwise, but if by steam at a pressure of from 125 to 200 pounds, the s eed of assage of the material between them einga actor.
- a feeding device referably in the form of a pair of driven eed rolls, which draw the material all the way from its source at the feed end of the machine through the platens, past a slitting and trimming device located between the p atens and the hardening oven, and through the hardening oven.
- the sheet may be severed by a suitable cutting device into the desired lengths.
- This oven also contains heated air, preferably in circulation.
- the sheet becomes a finished product, and is cooled and subject to safe manipulation.
- I preferably connect up the hot air supply so that the current therefrom heats both ovens serially, and I also prefer to arrange the platens and ovens in such manner that heat is conserved, and wasteful radiation avoided.
- 1 indicates a suitable bed or base frame having at the feed end thereof paper rolls 2 and 3 for the supply of liners.
- the plastic material is fed from a conventionally shown hopper 4 between rolls 5 and 6 beneath it.
- the paper from roll 2 passes over the top of roll 6 and thence around and under it in a reverse direction.
- the paper from roll 3 passes over roll 5 and thence under roll 6 continuing in the same direction, so that the plastic material is deposited in suitable quantities between thev two liners X and Y, and is held between them as the three-ply mass passes into the platen section.
- the platens of this section are made of a plurality of upper units 7 and lower units 8 spaced apart for the desired thickness, and the section is shown collectively in Figs. 1 and 2.
- Figs. 1 and 2 As the sheet emerges as shown at XY from the end of this section, its'edges are trimmed by suitable trimming devices 9, and it may be slit by another cutter indicated conventionally at 10 in Fig. 4 into two strips, if desired. It then immediately passes into the oven 11 shown collectively in -1gs. 2 and 3, where the hardening takes place.
- the feed rollers 12 suitably driven, which pull the sheet through all of the travel above described to this point.
- a continuation of the said lower ramp 15 within the processing or drying and curing oven 18 carries the sheet forwardly again through that oven, which is located immediately below the platen bed preferably in such manner that one tends to warm the other. Emerging at the forward end of oven 18 the sheet or board is again reversed by falling upon an incline of ramp 19 and carried on the latter back through the drying oven again. Its upper and lower paths in a reverse direction are shown in section in Fig. 6, 20 indicating 'a bafile between the two ramps.
- This lower ramp 19 issues from the opposite end of the oven, and finally delivers the board as a finished product at the rear end of the machine.
- the hot air supply for the oven is best shown in Figs. 3 and 4, and consists of an intake conduit 21 connected with a suitable heater and blower (not shown) which delivers into the drying oven 18. From thence it passes through a connection 22 into a conduit 23 and part of it goes through a connection 24 into the hardening oven 11, from which it emerges, all as shown by the arrows, at 25.
- This exhaust may be used in preliminarily treating some of the materials, or may go back to the heater. The remainder of the air current continues to traverse the conduit 1 23 emerging at 26, at which point it may be led back to the heater.
- Figs. 9, 10, 11 and 12 I have shown a modified form-of machinery which, up to the severing points 13, is substantially the same as the first embodiment.
- the board in this case passes up an inclined ramp 14a (Fig. 12) onto a shifting or tilting ramp 15a, the two positions of which are shown in full and dotted lines.
- This ramp carries suitably driven rollers, and delivers a length of board first to a lower ramp conveyer 16a in the dryer 18. It is reversed at the opposite end onto an upper ramp conveyer 19a by another tilting ramp 19?) as shown in Fig. 9. It is delivered at the rear end onto the platform 27, and there disposed of.
- a machine for forming sheets from plastics the combination with a pair of heated platen walls of substantial area, of means for feeding plastic material between said walls, a hardening oven associated with the platens and closely adjacent thereto, a drying and curing oven, and a feeding device located between the two ovens adapted to draw the hardened sheet from the first and to move it into the second, one of said ovens being relatively arranged to overlie the other.
- a machine for forming sheets from plastics the combination with a pair of heated platen walls of substantial area, of means for feeding plastic material between said walls, a hardening oven associated with the platens and closely adjacent-thereto, a drying and curingoven, and a feeding device located between the two ovens adapted to draw the hardenedsheet from the first and K to move it into the second, one of said ovens and the platens being relatively arranged to overlie each other.
- Apparatus for forming sheets of building material substantially continuously comprising means for forming a continuous strip of material, platen means for confining and heating a moving strip of said material, oven means for additionally heating said material, mechanism for pulling a continuous strip of said material through said platen means and oven means, severing mechanism beyond said pulling mechanism for severing said continuous strip into a plurality of separate panels, a treating chamber arranged in overlapping relation to said oven means so that the total length of said apparatus is reduced,
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Mechanical Engineering (AREA)
- Structural Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Devices For Post-Treatments, Processing, Supply, Discharge, And Other Processes (AREA)
- Treatment Of Fiber Materials (AREA)
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US246345A US1854872A (en) | 1928-01-12 | 1928-01-12 | Manufacture of sheets or slabs |
| NL45740A NL28914C (nl) | 1928-01-12 | 1929-04-05 | Werkwijze en inrichting voor het vervaardigen van muurplaten van plastisch materiaal |
| DEU10703A DE579719C (de) | 1928-01-12 | 1929-04-20 | Maschine zur Herstellung von Bauplatten |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US246345A US1854872A (en) | 1928-01-12 | 1928-01-12 | Manufacture of sheets or slabs |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| US1854872A true US1854872A (en) | 1932-04-19 |
Family
ID=22930273
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| US246345A Expired - Lifetime US1854872A (en) | 1928-01-12 | 1928-01-12 | Manufacture of sheets or slabs |
Country Status (3)
| Country | Link |
|---|---|
| US (1) | US1854872A (enExample) |
| DE (1) | DE579719C (enExample) |
| NL (1) | NL28914C (enExample) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE881473C (de) * | 1949-10-08 | 1953-06-29 | Wilhelm Dr-Ing Ludowici | Verfahren und Vorrichtung zum Pressen elastischer Massen |
| DE1081647B (de) * | 1954-06-10 | 1960-05-12 | Isoleringsaktiebolaget Wmb | Waermedaemmende Bautafel mit Stossverbindung |
-
1928
- 1928-01-12 US US246345A patent/US1854872A/en not_active Expired - Lifetime
-
1929
- 1929-04-05 NL NL45740A patent/NL28914C/nl active
- 1929-04-20 DE DEU10703A patent/DE579719C/de not_active Expired
Also Published As
| Publication number | Publication date |
|---|---|
| NL28914C (nl) | 1933-02-15 |
| DE579719C (de) | 1933-06-30 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US3200181A (en) | Method of and means for manufacturing padding and insulating materials comprising fibres | |
| US2366673A (en) | Method of preparing gypsum casts | |
| US2655458A (en) | Method of forming wood wool panels | |
| US1578250A (en) | Process of making plaster board | |
| US2069589A (en) | Machine for manufacturing pavements from vulcanizable materials | |
| ES491378A0 (es) | Un metodo,con su aparato correspondiente para la fabricacionde productos plasticos | |
| US1730673A (en) | Method and apparatus for producing a variegated plastic sheet | |
| US2344601A (en) | Treatment of fibrous glass | |
| BG99828A (bg) | Метод и инсталация за производството на изолационна лента от минерални влакна | |
| US4047865A (en) | Apparatus making pressed board | |
| AU631237B2 (en) | Process for producing panels or webs of laminated cellular thermoplastic material | |
| US2631381A (en) | Apparatus for making wallboard | |
| US2612706A (en) | Continuous manufacture of extruded clay composition bodies | |
| US2742951A (en) | Art of curling or kinking stretched filaments and forming pads therefrom | |
| US2173391A (en) | Process of manufacturing fibrous products | |
| US1829802A (en) | Machine and method for making wall board | |
| US1655714A (en) | Machine and method for making wall board | |
| KR100358071B1 (ko) | 매트 솜의 제조방법 및 그 장치 | |
| US1803779A (en) | Platen support for heat processing machines | |
| US2263207A (en) | Intermittent conveyer | |
| JP2859687B2 (ja) | 陶板の製造方法 | |
| US1803780A (en) | Platen mechanism for heat processing machines | |
| US2134659A (en) | Synthetic fibrous product and process of making the same | |
| US1819199A (en) | Method of making building materials | |
| JPS6317250A (ja) | 長尺陶板の連続製造装置 |