EP4327672B1 - Preparation method for multi-section aerosol generating product - Google Patents
Preparation method for multi-section aerosol generating product Download PDFInfo
- Publication number
- EP4327672B1 EP4327672B1 EP22865875.3A EP22865875A EP4327672B1 EP 4327672 B1 EP4327672 B1 EP 4327672B1 EP 22865875 A EP22865875 A EP 22865875A EP 4327672 B1 EP4327672 B1 EP 4327672B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- aerosol generating
- generating material
- accommodating cavity
- cavity
- composite tube
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/02—Manufacture of tobacco smoke filters
- A24D3/0229—Filter rod forming processes
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D1/00—Cigars; Cigarettes
- A24D1/20—Cigarettes specially adapted for simulated smoking devices
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24B—MANUFACTURE OR PREPARATION OF TOBACCO FOR SMOKING OR CHEWING; TOBACCO; SNUFF
- A24B15/00—Chemical features or treatment of tobacco; Tobacco substitutes, e.g. in liquid form
- A24B15/10—Chemical features of tobacco products or tobacco substitutes
- A24B15/16—Chemical features of tobacco products or tobacco substitutes of tobacco substitutes
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24C—MACHINES FOR MAKING CIGARS OR CIGARETTES
- A24C5/00—Making cigarettes; Making tipping materials for, or attaching filters or mouthpieces to, cigars or cigarettes
- A24C5/01—Making cigarettes for simulated smoking devices
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/02—Manufacture of tobacco smoke filters
- A24D3/025—Final operations, i.e. after the filter rod forming process
- A24D3/0254—Cutting means
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/04—Tobacco smoke filters characterised by their shape or structure
- A24D3/048—Tobacco smoke filters characterised by their shape or structure containing additives
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24F—SMOKERS' REQUISITES; MATCH BOXES; SIMULATED SMOKING DEVICES
- A24F40/00—Electrically operated smoking devices; Component parts thereof; Manufacture thereof; Maintenance or testing thereof; Charging means specially adapted therefor
- A24F40/20—Devices using solid inhalable precursors
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24F—SMOKERS' REQUISITES; MATCH BOXES; SIMULATED SMOKING DEVICES
- A24F40/00—Electrically operated smoking devices; Component parts thereof; Manufacture thereof; Maintenance or testing thereof; Charging means specially adapted therefor
- A24F40/40—Constructional details, e.g. connection of cartridges and battery parts
- A24F40/42—Cartridges or containers for inhalable precursors
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24F—SMOKERS' REQUISITES; MATCH BOXES; SIMULATED SMOKING DEVICES
- A24F40/00—Electrically operated smoking devices; Component parts thereof; Manufacture thereof; Maintenance or testing thereof; Charging means specially adapted therefor
- A24F40/70—Manufacture
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/02—Manufacture of tobacco smoke filters
- A24D3/0275—Manufacture of tobacco smoke filters for filters with special features
- A24D3/0287—Manufacture of tobacco smoke filters for filters with special features for composite filters
Definitions
- the present disclosure belongs to a heat-not-burn (HNB) cigarette field, and in particular, to a preparation method of multi-sectional aerosol generating products (see for example WO 2022/016714 A1 ).
- HNB heat-not-burn
- Aerosol generating matrix of granular heating cigarette is bulk aerosol generating granules
- in the prior art as bulk aerosol generating granules cannot be fixed, they must be filled into the outer tube by filling, besides, both sides of the aerosol generating granule section are sealed by sealing paper and plugging part to fix granules, while in order to gather aerosol and increase the amount of smoke, the downstream of the plugging part is usually a section of cavity (a cavity section) limited by the outer tube, and the downstream of the cavity section is a filtering section.
- the above aerosol generating products are prepared by filling, the production process order is as follows: one end of the tube is sealed, while aerosol generating matrix, the plugging part and the filtering part are sequentially filled from the other end, when filling the filtering part, a cavity distance between the filtering part and the plugging part is reserved, and the outer surface of the plugging part and the filtering part is not glued to the inner wall of the paper tube, after direct filling to a fixed position, they are fixed by friction with the inner wall of the paper tube.
- the present disclosure is proposed to solve the problems above.
- the present disclosure uses a rolling and compounding method to form each unit except the aerosol generating granule section, and a cavity for filling the aerosol generating material is reserved during compounding, cutting is carried out as needed after compounding, and the cut filter tip with an aerosol generating matrix accommodating cavity is placed vertically, then the aerosol generating material is filled into the aerosol generating matrix accommodating cavity, the method of compounding before filling of the present disclosure can greatly improve production efficiency, and ensure that the plugging part 2 and the filtering part 4 are stable without moving during smoking or transportation, and better maintain consistency of axial lengths of the cavity section of different samples.
- the present disclosure provides a preparation method of multi-sectional aerosol generating products, including the following steps:
- the flowing aerosol generating material can be filled into the aerosol generating matrix accommodating 5 in any way, e.g., squeezing;
- preparation of the filter-tip rod can be in a horizontal, vertical or any state between the two, as long as the filter-tip rod is placed in a vertical state during filling of aerosol generating materials in step 2, so as to facilitate quantitative squeezing of the flowing aerosol generating material.
- the purpose of drying and expanding at a certain temperature on the plane after inversion is to make the end face of the aerosol generating rod 6 far away from the filtering part even.
- the filter-tip rod can be cut into a plurality of filter tips, and the plurality of filter tips are connected by the filtering part 4 and / or the aerosol generating matrix accommodating cavity 5; at this time, there is also a cutting step between step 1 and step 2, which is to cut at the connected filtering part 4 and / or the connected aerosol generating matrix accommodating cavity 5, to cut the filter-tip rod into a plurality of filter tips.
- the filter-tip rod in step 1 can be a separate filter tip, that is, the composite tube 1 includes a plugging part 2, a cavity section 3, a filtering part 4 and an aerosol generating matrix accommodating cavity 5; in this case, when step 2 is carried out, it is only necessary to place the aerosol generating matrix accommodating cavity 5 vertically upward.
- the filter-tip rod in step 1 can be cut into a plurality of filter tips, that is, the composite tube 1 includes a plugging part 2, a cavity section 3, a filtering part 4 and an aerosol generating matrix accommodating cavity 5, and the plurality of filter tips are connected by the filtering part 4 and / or the aerosol generating matrix accommodating cavity 5, the junction has twice the axial length of the filtering part 4 or the aerosol generating matrix accommodating cavity 5, in this case, when step 2 is carried out, it is also necessary to cut the filter-tip rod into a plurality of filter tips, and place the aerosol generating matrix accommodating cavity 5 vertically upward.
- the axial length of the filtering part at the junction is twice that of the filtering part in a single filter tip; similarly, the axial length of the aerosol generating matrix accommodating cavity reserved at the junction is twice that of the aerosol generating matrix accommodating cavity in a single filter tip, so that each filter tip has a complete filtering part and an aerosol generating matrix accommodating cavity after cutting.
- the flowing aerosol generating material includes smoking raw materials, smoking agents and solvents, the smoking raw materials are crushed in advance and passed through a 40-200 mesh sieve, the smoking raw materials after sieving are mixed separately with smoking agents and solvents in a certain proportion to form a flowing aerosol generating material like plaster;
- the filling amount of the flowing aerosol generating material is 50-95 % of volume of the aerosol generating matrix accommodating cavity 5, more preferably, 90%.
- step 2 there is a binder in the flowing aerosol generating material, the flowing aerosol generating material is bonded to the inner wall of the composite tube 1 with its own binder during drying and expansion.
- the binder is selected from chitosan, ethyl cellulose with hydroxyethylation compound modification, guar gum, carboxymethyl cellulose, starch, modified starch, plant cellulose, microcrystalline cellulose, hydroxyethyl cellulose, hydroxyethyl methyl cellulose.
- step 2 the flowing aerosol generating material is squeezed into the aerosol generating matrix accommodating cavity 5 while cleaving to the inner surface of the composite tube 1, and the squeezed flowing aerosol generating material forms a central cavity, the center is the volume reserved for expansion of aerosol generating materials; or,
- the flowing aerosol generating material is filled into the aerosol generating matrix accommodating cavity 5 in two parts, wherein, a first part of the aerosol generating material is squeezed into the aerosol generating matrix accommodating cavity 5 while cleaving to the inner surface of the composite tube 1, the first part of the squeezed aerosol generating material forms a central cavity, and a second part of the aerosol generating material is squeezed into the central cavity, there is a gap between the first part of the aerosol generating material and the second part of the aerosol generating material, the gap is the volume reserved for expansion of aerosol generating materials.
- step 2 there is also a sealing step after step 2 to make the aerosol generating matrix accommodating cavity 5 filled with the aerosol generating matrix 6 far away from the end surface of the filtering section to form a sealing film.
- step 2 determines whether the sealing film is needed according to conditions of the aerosol generating matrix 6.
- drying temperature in step 3 depends on the solvent in the aerosol generating material, i.e., in case the solvent is ethanol, the drying temperature is 50-60 °C , with drying time of 0.5-1h; in case the solvent is water, the drying temperature is 60-70°C, with drying time of 1-2h.
- the cavity section 3 also includes functional materials; and / or, the cavity section 3 also includes an empty-tube fitting, the wall of the empty-tube fitting 32 is made of paper, silica gel, cellulose acetate, polylactic acid and non-woven fabric.
- Functional materials can be any form of material with cooling and flavoring function in the prior art.
- the air vent 31 is provided on the composite tube 1 in the cavity section 3 that radially penetrates through the composite tube 1.
- the air vent 31 penetrates through the composite tube 1 and the empty-tube fitting at the same time.
- the air vent 31 is to introduce air into the cavity section, so as to reduce aerosol temperature and suction resistance, thus, to determine whether the vent 31 is needed according to actual aerosol temperatures and suction resistance.
- perforating is used to form the air vent, certainly, it is also possible to use permeable paper as a composite tube or an empty-paper pipe in the cavity section without perforating, as long as air can be introduced into the cavity section.
- the binder is selected from ordinary lap adhesive.
- the composite tube 1 is made of paper and a non-woven fabric.
- the water-proof layer is made of alkyl ketene dimer (AKD), cationic rosin gum, non-iron aluminum sulfate mix or paraffin material;
- the oil-proof layer is made of fluorocarbon organic matter, modified starch, AKD and paraffin mixture, AKD and modified starch mixture material.
- the heat-conduction layer is selected from but not limited to an aluminum foil layer, which is added to the inner wall of the cigarette paper tube by paste; the aluminum foil layer can play the role of water-proof and / or oil-proof, while conducting and preserving heat, so that the smoking material in the inner wall of the cigarette is evenly heated.
- the water-proof layer and / or oil-proof layer are coated on the inner wall of the cigarette paper tube by spraying.
- the water-proof layer is made of alkyl ketene dimer (AKD), cationic rosin gum or non-iron aluminum sulfate mix and paraffin material, so as to prevent moisture in the smoking material from seeping to the outside of the cigarette paper tube.
- ALD alkyl ketene dimer
- cationic rosin gum or non-iron aluminum sulfate mix and paraffin material
- smoking agents, flavors and fragrances are added to smoking materials, during long-term placement, smoking agents in the smoking materials may carry flavors and fragrances to seep to the outside of the paper tube, resulting in yellow spots and affecting appearances of paper tubes, as smoking agents are oily, it is necessary to add an oil-proof layer to the inner wall of the cigarette paper tube filled with smoking materials.
- the oil-proof layer is made of fluorocarbon organic matter, modified starch, AKD and paraffin mixture, AKD and modified starch mixture, so as to prevent smoking agents in smoking material carrying flavors and fragrances to seep to the outside of the paper tube and occurrence of yellow spots.
- the plugging part can be in any form, as long as blocking aerosol generating matrix (6) from moving downstream.
- a plurality of means two or more.
- the orientation or state relationship indicated by the terms “inside”, “above”, “below”, etc. is based on that shown in the figures, which is only for convenience of describing the present disclosure and simplifying description, rather than indicating or implying that the device or element must have a particular orientation, or must be constructed and operated in a particular orientation, and thus should not be interpreted as limitations of the present disclosure.
- the embodiment provides a preparation method of multi-sectional aerosol generating products, including the following steps:
- step 2 the flowing aerosol generating material is filled into the aerosol generating matrix accommodating cavity 5 by squeezing; in step 1, preparation of filter-tip rod is in a horizontal state by existing compounding machines.
- step 1 the filter-tip rod can be cut into two filter tips, and the two filter tips are connected by aerosol generating matrix accommodating cavity 5; at this time, there is also a cutting step between step 1 and step 2, which is to cut at the connected aerosol generating matrix accommodating cavity 5, so as to cut the filter-tip rod into two filter tips.
- the joint has twice the axial length of the aerosol generating matrix accommodating cavity 5, so that each filter-tip rod has a complete aerosol generating matrix accommodating cavity after cutting.
- the flowing aerosol generating material includes smoking raw materials, smoking agents and solvents, the smoking raw materials are crushed in advance and passed through a 40-200 mesh sieve, the smoking raw materials after sieving are mixed separately with smoking agents and solvents in a certain proportion to form a flowing aerosol generating material like plaster;
- the filling amount of the flowing aerosol generating material is 90% of volume of the aerosol generating matrix accommodating cavity 5.
- step 2 there is a binder in the flowing aerosol generating material, the flowing aerosol generating material is bonded to the inner wall of the composite tube 1 with its own binder during drying and expansion.
- the binder is selected from carboxymethyl cellulose.
- step 2 the flowing aerosol generating material is squeezed into the aerosol generating matrix accommodating cavity 5 while cleaving to the inner surface of the composite tube 1, and the squeezed flowing aerosol generating material forms a central cavity, the center is the volume reserved for expansion of aerosol generating materials.
- the drying temperature depends on the solvent in the aerosol generating material, in the embodiment, the solvent is water, the drying temperature is 60 °C with drying time of 1h.
- the cavity section 3 also includes an empty-tube fitting, the empty-tube fitting can be empty paper tube.
- the composite tube 1 in the cavity section 3 has an air vent 31 that penetrates radially through the composite tube 1. In case an empty-tube fitting is provided in the cavity section 3, the air vent 31 runs through the composite tube 1 and the empty-tube fitting at the same time.
- the composite tube 1 is made of paper.
- step 1 the filter-tip rod can be cut into four filter tips, and the four filter tips are connected by the filtering part 4 and the aerosol generating matrix accommodating cavity 5; at this time, there is also a cutting step between step 1 and step 2, which is to cut at the connected filtering part 4 and the connected aerosol generating matrix accommodating cavity 5, so as to cut the filter-tip rod into 4 filter tips.
- the axial length of the filtering part at the junction is twice that of the filtering part in a single filter-tip; similarly, the axial length of the aerosol generating matrix accommodating cavity reserved at the junction is twice that of the aerosol generating matrix accommodating cavity in a single filter-tip, so that each filter rod has a complete filtering part and an aerosol generating matrix accommodating cavity after cutting.
- step 2 the flowing aerosol generating material is filled into the aerosol generating matrix accommodating cavity 5 in two parts, wherein, a first part of the aerosol generating material is squeezed into the aerosol generating matrix accommodating cavity 5 while cleaving to the inner surface of the composite tube 1, the first part of the squeezed aerosol generating material forms a central cavity, and a second part of the aerosol generating material is squeezed into the central cavity, there is a gap between the first part of the aerosol generating material and the second part of the aerosol generating material, the gap is the volume reserved for expansion of aerosol generating materials.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Cigarettes, Filters, And Manufacturing Of Filters (AREA)
- Containers And Packaging Bodies Having A Special Means To Remove Contents (AREA)
- Manufacturing Of Micro-Capsules (AREA)
Description
- The present disclosure belongs to a heat-not-burn (HNB) cigarette field, and in particular, to a preparation method of multi-sectional aerosol generating products (see for example
WO 2022/016714 A1 ). - With increasing attention of consumers to health and increasing demand for personalized experiences of cigarette products, the tobacco industry has continuously responded to upgrading of consumers' needs, various smoking products with tar reduction have been developed so as to bring less harm to consumers. Among which, because of different heating methods compared with traditional cigarette products, heating cigarettes can provide a healthier smoking experience while meeting consumers' sensory needs for cigarette products.
- Aerosol generating matrix of granular heating cigarette is bulk aerosol generating granules, in the prior art, as bulk aerosol generating granules cannot be fixed, they must be filled into the outer tube by filling, besides, both sides of the aerosol generating granule section are sealed by sealing paper and plugging part to fix granules, while in order to gather aerosol and increase the amount of smoke, the downstream of the plugging part is usually a section of cavity (a cavity section) limited by the outer tube, and the downstream of the cavity section is a filtering section.
- At present, the above aerosol generating products are prepared by filling, the production process order is as follows: one end of the tube is sealed, while aerosol generating matrix, the plugging part and the filtering part are sequentially filled from the other end, when filling the filtering part, a cavity distance between the filtering part and the plugging part is reserved, and the outer surface of the plugging part and the filtering part is not glued to the inner wall of the paper tube, after direct filling to a fixed position, they are fixed by friction with the inner wall of the paper tube.
- Problem of the above filling method are as follows: 1. The tube is placed vertically during filling, and it is difficult to locate positions of the plugging part and the filtering part on both sides of the cavity, resulting in inconsistent axial lengths of the cavity section of different samples; 2. As the outer surface of the plugging part and filtering part and the inner wall of the paper tube are fixed only by friction, during transportation, the plugging part and filtering part are easy to move toward the cavity section, or the filtering part is partially sucked out of the outer tube during smoking; 3. The filling method is limited in that it can only be filled in batches for individual tubes, resulting in low production efficiency.
- Therefore, efficient production of granular aerosol generating products with a cavity structure, while ensuring stability of the plugging and filtering parts without moving are key problems to be solved in production of granular aerosol generating products.
- The present disclosure is proposed to solve the problems above.
- The present disclosure uses a rolling and compounding method to form each unit except the aerosol generating granule section, and a cavity for filling the aerosol generating material is reserved during compounding, cutting is carried out as needed after compounding, and the cut filter tip with an aerosol generating matrix accommodating cavity is placed vertically, then the aerosol generating material is filled into the aerosol generating matrix accommodating cavity, the method of compounding before filling of the present disclosure can greatly improve production efficiency, and ensure that the plugging
part 2 and the filteringpart 4 are stable without moving during smoking or transportation, and better maintain consistency of axial lengths of the cavity section of different samples. - The present disclosure provides a preparation method of multi-sectional aerosol generating products, including the following steps:
-
Step 1, preparation of filter-tip rod:- A
composite tube 1 is used to wrap aplugging part 2 and afiltering part 4, a first axial length of the interval between theplugging part 2 and thefiltering part 4, the length is acavity section 3 limited by thecomposite tube 1, - One end of plugging
part 2 far away from thecavity section 3 is an aerosol generating matrix accommodatingcavity 5 limited by thecomposite tube 1;
- A
-
Step 2, filling of aerosol generating material:
The filter-tip rod is in a vertical state, that is, perpendicular to the horizontal plane, wherein, the aerosol generating matrix accommodatingcavity 5 is vertically upward, and the flowing aerosol generating material is squeezed into the aerosol generating matrix accommodatingcavity 5; -
Step 3, forming of aerosol generating rod 6:
Rotate the filter-tip rod filled with aerosol generating material by 180° , so that the aerosol generating matrix accommodatingcavity 5 is vertically downward, place it on the plane to dry and expand at a certain temperature, so that the aerosol generating material is solidified to form a fixedaerosol generating rod 6 in the aerosol generating matrix accommodatingcavity 5. - In
step 2, the flowing aerosol generating material can be filled into the aerosol generating matrix accommodating 5 in any way, e.g., squeezing;
Instep 1, preparation of the filter-tip rod can be in a horizontal, vertical or any state between the two, as long as the filter-tip rod is placed in a vertical state during filling of aerosol generating materials instep 2, so as to facilitate quantitative squeezing of the flowing aerosol generating material. - The purpose of drying and expanding at a certain temperature on the plane after inversion is to make the end face of the
aerosol generating rod 6 far away from the filtering part even. - Preferably, in
step 1, the filter-tip rod can be cut into a plurality of filter tips, and the plurality of filter tips are connected by the filteringpart 4 and / or the aerosol generating matrix accommodatingcavity 5; at this time, there is also a cutting step betweenstep 1 andstep 2, which is to cut at the connected filteringpart 4 and / or the connected aerosol generating matrix accommodatingcavity 5, to cut the filter-tip rod into a plurality of filter tips. - That is to say, the filter-tip rod in
step 1 can be a separate filter tip, that is, thecomposite tube 1 includes aplugging part 2, acavity section 3, a filteringpart 4 and an aerosol generating matrix accommodatingcavity 5; in this case, whenstep 2 is carried out, it is only necessary to place the aerosol generating matrix accommodatingcavity 5 vertically upward. - Certainly, the filter-tip rod in
step 1 can be cut into a plurality of filter tips, that is, thecomposite tube 1 includes aplugging part 2, acavity section 3, a filteringpart 4 and an aerosol generatingmatrix accommodating cavity 5, and the plurality of filter tips are connected by the filteringpart 4 and / or the aerosol generating matrix accommodatingcavity 5, the junction has twice the axial length of the filteringpart 4 or the aerosol generating matrix accommodatingcavity 5, in this case, whenstep 2 is carried out, it is also necessary to cut the filter-tip rod into a plurality of filter tips, and place the aerosol generating matrix accommodatingcavity 5 vertically upward. - That is to say, the axial length of the filtering part at the junction is twice that of the filtering part in a single filter tip; similarly, the axial length of the aerosol generating matrix accommodating cavity reserved at the junction is twice that of the aerosol generating matrix accommodating cavity in a single filter tip, so that each filter tip has a complete filtering part and an aerosol generating matrix accommodating cavity after cutting.
- Preferably, in
step 2, the flowing aerosol generating material includes smoking raw materials, smoking agents and solvents, the smoking raw materials are crushed in advance and passed through a 40-200 mesh sieve, the smoking raw materials after sieving are mixed separately with smoking agents and solvents in a certain proportion to form a flowing aerosol generating material like plaster; - Preferably, in
step 2, the filling amount of the flowing aerosol generating material is 50-95 % of volume of the aerosol generating matrix accommodatingcavity 5, more preferably, 90%. - Preferably, in
step 2, there is a binder in the flowing aerosol generating material, the flowing aerosol generating material is bonded to the inner wall of thecomposite tube 1 with its own binder during drying and expansion. The binder is selected from chitosan, ethyl cellulose with hydroxyethylation compound modification, guar gum, carboxymethyl cellulose, starch, modified starch, plant cellulose, microcrystalline cellulose, hydroxyethyl cellulose, hydroxyethyl methyl cellulose. - Preferably, in
step 2, the flowing aerosol generating material is squeezed into the aerosol generating matrix accommodatingcavity 5 while cleaving to the inner surface of thecomposite tube 1, and the squeezed flowing aerosol generating material forms a central cavity, the center is the volume reserved for expansion of aerosol generating materials; or, - The flowing aerosol generating material is filled into the aerosol generating matrix accommodating
cavity 5 in two parts, wherein, a first part of the aerosol generating material is squeezed into the aerosol generating matrix accommodatingcavity 5 while cleaving to the inner surface of thecomposite tube 1, the first part of the squeezed aerosol generating material forms a central cavity, and a second part of the aerosol generating material is squeezed into the central cavity, there is a gap between the first part of the aerosol generating material and the second part of the aerosol generating material, the gap is the volume reserved for expansion of aerosol generating materials. - Preferably, there is also a sealing step after
step 2 to make the aerosol generating matrix accommodatingcavity 5 filled with theaerosol generating matrix 6 far away from the end surface of the filtering section to form a sealing film. In actual production processes, determine whether the sealing film is needed according to conditions of theaerosol generating matrix 6. - Preferably, in
step 3, drying temperature instep 3 depends on the solvent in the aerosol generating material, i.e., in case the solvent is ethanol, the drying temperature is 50-60 °C , with drying time of 0.5-1h; in case the solvent is water, the drying temperature is 60-70°C, with drying time of 1-2h. - Preferably, the
cavity section 3 also includes functional materials; and / or, thecavity section 3 also includes an empty-tube fitting, the wall of the empty-tube fitting 32 is made of paper, silica gel, cellulose acetate, polylactic acid and non-woven fabric. Functional materials can be any form of material with cooling and flavoring function in the prior art. - Preferably, the
air vent 31 is provided on thecomposite tube 1 in thecavity section 3 that radially penetrates through thecomposite tube 1. In case the empty-tube fitting is provided within the cavity section, theair vent 31 penetrates through thecomposite tube 1 and the empty-tube fitting at the same time. Theair vent 31 is to introduce air into the cavity section, so as to reduce aerosol temperature and suction resistance, thus, to determine whether thevent 31 is needed according to actual aerosol temperatures and suction resistance. In case theair vent 31 is needed, preferably, perforating is used to form the air vent, certainly, it is also possible to use permeable paper as a composite tube or an empty-paper pipe in the cavity section without perforating, as long as air can be introduced into the cavity section. - Preferably, there is a binder between the outer surface of the plugging
part 2 and the inner surface of thecomposite tube 1, and there is a binder between the outer surface of thefiltering part 4 and the inner surface of thecomposite tube 1. The binder is selected from ordinary lap adhesive. - Preferably, the
composite tube 1 is made of paper and a non-woven fabric. The anti-seepage / heat-conduction layer with anti-seepage or heat-conduction function on the composite tube 1 (especially when thecomposite tube 1 is made of non-woven fabric), the anti-seepage / heat-conduction layer includes a water-proof layer and / or an oil-proof layer and / or a heat-conduction layer; - The water-proof layer is made of alkyl ketene dimer (AKD), cationic rosin gum, non-iron aluminum sulfate mix or paraffin material; the oil-proof layer is made of fluorocarbon organic matter, modified starch, AKD and paraffin mixture, AKD and modified starch mixture material. The heat-conduction layer is selected from but not limited to an aluminum foil layer, which is added to the inner wall of the cigarette paper tube by paste; the aluminum foil layer can play the role of water-proof and / or oil-proof, while conducting and preserving heat, so that the smoking material in the inner wall of the cigarette is evenly heated.
- Preferably, the water-proof layer and / or oil-proof layer are coated on the inner wall of the cigarette paper tube by spraying.
- As moisture in the smoking material during cigarette storage seeps to the outside of the cigarette paper tube and results in yellow spots, it is necessary to add a water-proof layer to the inner wall of the cigarette paper tube filled with smoking material. The water-proof layer is made of alkyl ketene dimer (AKD), cationic rosin gum or non-iron aluminum sulfate mix and paraffin material, so as to prevent moisture in the smoking material from seeping to the outside of the cigarette paper tube.
- Similarly, smoking agents, flavors and fragrances are added to smoking materials, during long-term placement, smoking agents in the smoking materials may carry flavors and fragrances to seep to the outside of the paper tube, resulting in yellow spots and affecting appearances of paper tubes, as smoking agents are oily, it is necessary to add an oil-proof layer to the inner wall of the cigarette paper tube filled with smoking materials. The oil-proof layer is made of fluorocarbon organic matter, modified starch, AKD and paraffin mixture, AKD and modified starch mixture, so as to prevent smoking agents in smoking material carrying flavors and fragrances to seep to the outside of the paper tube and occurrence of yellow spots.
- The plugging part can be in any form, as long as blocking aerosol generating matrix (6) from moving downstream.
- Compared with the prior art, the present disclosure has the following beneficial effects:
- 1. The present disclosure uses a rolling and compounding method to form each unit except the aerosol generating granule section, and a cavity for filling the aerosol generating material is reserved during compounding, cutting is carried out as needed after compounding, and the cut filter tip with an aerosol generating matrix accommodating
cavity 5 is placed vertically, then the aerosol generating material is filled into the aerosol generating matrix accommodatingcavity 5, as theplugging part 2 and the filteringpart 4 are formed by compounding and rolling, it is easier to locate the pluggingpart 2 and the filteringpart 4 in axial positions, to better ensure consistency of axial lengths of thecavity section 3 of different samples.
As the pluggingpart 2 and the filteringpart 4 are formed by compounding and rolling, it is more convenient to apply a binder between the outer surface of theplugging part 2 and the filteringpart 4 and the inner surface of the paper tube, so as to ensure that no displacement occurs at both ends during smoking or transportation. - 2. The present disclosure uses the method of compounding and then filling to prepare aerosol generating products, which can simultaneously compound a plurality of filter tips, then cut and fill the aerosol generating material, as other units are compounded except the aerosol generating material, efficiency of each unit is greatly improved compared with separate filling.
- 3. In the present disclosure, the flowing aerosol generating material is filled by squeezing, places the aerosol generating matrix accommodating
cavity 5 vertically downward on the plane to dry and expand at a certain temperature, so that the aerosol generating material is solidify to form a fixedaerosol generating rod 6 located in the aerosol generating matrix accommodatingcavity 5, production efficiency is higher by squeezing, and theaerosol generating rod 6 obtained after drying and expanding has a pore structure, which can facilitate release and circulation of aerosol. The purpose of drying and expanding at a certain temperature on the plane after inversion is to make the end face of theaerosol generating rod 6 far away from the filtering part even. -
-
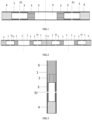
FIG.1 is a structural schematic view of a filter-tip rod with two filter tips before cutting inEmbodiment 1, the dotted line in the figure is the cutting position. -
FIG.2 is a structural schematic view of a filter-tip rod with three filter tips before cutting inEmbodiment 1, the dotted line in the figure is the cutting position. -
FIG.3 is a structural schematic view of the aerosol generating products obtained. - List of the reference signs of figures in the description of
figures: 1 . Composite tube, 2. Plugging part, 3. Cavity section, 4. Filtering part, 5. Aerosol generating matrix accommodating cavity, 6. Aerosol generating rod, 31. Air vent. - The present disclosure is further illustrated through specific embodiments.
- It is understood by those skilled in the art that, the following embodiments are only for illustrating the present disclosure and should not be interpreted as limiting the scope of the present disclosure. In case no specific technique or condition is indicated in the embodiment, the technique or condition described in the literature in the field or the product specification is based on. In case the materials or equipment used are not indicated with manufacturers, they are all ordinary products that can be obtained through purchase.
- It can be understood by those skilled in the art that, the singular forms "a", "an" and "the" used herein can include the plural forms as well, unless expressly stated otherwise. It should be further understood that "including" used in the description of the present disclosure means that the features, integers, steps, operations, elements and/or components exist; however, the existence or addition of one or more other features, integers, steps, operations, elements, components and/or groups thereof is not excluded. It should be understood that, when an element is referred to be "connected" to another one, it may be directly connected to another element, or there may be intermediate elements as well. Moreover, "connection" as used herein may include wireless connections.
- In the description of the present disclosure, unless otherwise stated, "a plurality of" means two or more. The orientation or state relationship indicated by the terms "inside", "above", "below", etc. is based on that shown in the figures, which is only for convenience of describing the present disclosure and simplifying description, rather than indicating or implying that the device or element must have a particular orientation, or must be constructed and operated in a particular orientation, and thus should not be interpreted as limitations of the present disclosure.
- In the description of the present disclosure, it should be noted that, the terms "mount", "connect" and "provided with" should be interpreted broadly unless otherwise expressly specified and defined, such as fixed connection, detachable connection, or integral connection; either mechanical connection or electrical connection; direct connection or indirect connection through intermediate media. The specific meanings of the terms above in the present disclosure can be understood by persons skilled in the art in actual conditions.
- It is understood by those skilled in the art that, unless otherwise defined, all terms including technical and scientific terms used herein have the same meanings as commonly understood by the ordinary persons skilled in the art to the technical field to which the present disclosure belongs. It should also be understood that terms such as those defined in the general dictionary should be understood to have meanings consistent with those in the context of the prior art; moreover, unless defined as herein, the terms may not be explained with idealized or overly formal senses.
- The embodiment provides a preparation method of multi-sectional aerosol generating products, including the following steps:
-
Step 1, preparation of filter-tip rod:- A
composite tube 1 is used to wrap a pluggingpart 2 and afiltering part 4, there is a first axial length of the interval between the pluggingpart 2 and thefiltering part 4, the length is acavity section 3 limited by thecomposite tube 1, - One end of plugging
part 2 far away from thecavity section 3 is an aerosol generating matrixaccommodating cavity 5 limited by thecomposite tube 1;
- A
-
Step 2, filling of aerosol generating material:
The filter-tip rod is in a vertical state, that is, perpendicular to the horizontal plane, wherein, the aerosol generating matrixaccommodating cavity 5 is vertically upward, and the flowing aerosol generating material is squeezed into the aerosol generating matrixaccommodating cavity 5; -
Step 3, forming of aerosol generating rod 6:
Rotate the filter-tip rod filled with aerosol generating material by 180° , so that the aerosol generating matrixaccommodating cavity 5 is vertically downward, place it on the plane to dry and expand at a certain temperature, so that the aerosol generating material is solidified to form a fixedaerosol generating rod 6 in the aerosol generating matrixaccommodating cavity 5. - In
step 2, the flowing aerosol generating material is filled into the aerosol generating matrixaccommodating cavity 5 by squeezing; instep 1, preparation of filter-tip rod is in a horizontal state by existing compounding machines. - In
step 1, the filter-tip rod can be cut into two filter tips, and the two filter tips are connected by aerosol generating matrixaccommodating cavity 5; at this time, there is also a cutting step betweenstep 1 andstep 2, which is to cut at the connected aerosol generating matrixaccommodating cavity 5, so as to cut the filter-tip rod into two filter tips. The joint has twice the axial length of the aerosol generating matrixaccommodating cavity 5, so that each filter-tip rod has a complete aerosol generating matrix accommodating cavity after cutting. - In
step 2, the flowing aerosol generating material includes smoking raw materials, smoking agents and solvents, the smoking raw materials are crushed in advance and passed through a 40-200 mesh sieve, the smoking raw materials after sieving are mixed separately with smoking agents and solvents in a certain proportion to form a flowing aerosol generating material like plaster;
Instep 2, the filling amount of the flowing aerosol generating material is 90% of volume of the aerosol generating matrixaccommodating cavity 5. - In
step 2, there is a binder in the flowing aerosol generating material, the flowing aerosol generating material is bonded to the inner wall of thecomposite tube 1 with its own binder during drying and expansion. The binder is selected from carboxymethyl cellulose. - In
step 2, the flowing aerosol generating material is squeezed into the aerosol generating matrixaccommodating cavity 5 while cleaving to the inner surface of thecomposite tube 1, and the squeezed flowing aerosol generating material forms a central cavity, the center is the volume reserved for expansion of aerosol generating materials. - In
step 3, the drying temperature depends on the solvent in the aerosol generating material, in the embodiment, the solvent is water, the drying temperature is 60 °C with drying time of 1h. - The
cavity section 3 also includes an empty-tube fitting, the empty-tube fitting can be empty paper tube. Thecomposite tube 1 in thecavity section 3 has anair vent 31 that penetrates radially through thecomposite tube 1. In case an empty-tube fitting is provided in thecavity section 3, theair vent 31 runs through thecomposite tube 1 and the empty-tube fitting at the same time. - There is a binder between the outer surface of the plugging
part 2 and the inner surface of thecomposite tube 1, and there is a binder between the outer surface of thefiltering part 4 and the inner surface of thecomposite tube 1. - The
composite tube 1 is made of paper. - The differences between
embodiment 2 andembodiment 1 are that, 1. Instep 1, the filter-tip rod can be cut into four filter tips, and the four filter tips are connected by thefiltering part 4 and the aerosol generating matrixaccommodating cavity 5; at this time, there is also a cutting step betweenstep 1 andstep 2, which is to cut at the connected filteringpart 4 and the connected aerosol generating matrixaccommodating cavity 5, so as to cut the filter-tip rod into 4 filter tips. The axial length of the filtering part at the junction is twice that of the filtering part in a single filter-tip; similarly, the axial length of the aerosol generating matrix accommodating cavity reserved at the junction is twice that of the aerosol generating matrix accommodating cavity in a single filter-tip, so that each filter rod has a complete filtering part and an aerosol generating matrix accommodating cavity after cutting. 2. Instep 2, the flowing aerosol generating material is filled into the aerosol generating matrixaccommodating cavity 5 in two parts, wherein, a first part of the aerosol generating material is squeezed into the aerosol generating matrixaccommodating cavity 5 while cleaving to the inner surface of thecomposite tube 1, the first part of the squeezed aerosol generating material forms a central cavity, and a second part of the aerosol generating material is squeezed into the central cavity, there is a gap between the first part of the aerosol generating material and the second part of the aerosol generating material, the gap is the volume reserved for expansion of aerosol generating materials.
Claims (10)
- A preparation method of multi-sectional aerosol generating products, wherein, the method comprises the following steps:Step 1, preparation of filter-tip rod:A composite tube (1) is used to wrap a plugging part (2) and a filtering part (4), there is a first axial length of the interval between the plugging part (2) and the filtering part (4), the length is a cavity section (3) limited by the composite tube (1),One end of plugging part (2) far away from the cavity section (3) is an aerosol generating matrix accommodating cavity (5) limited by the composite tube (1);Step 2, filling of an aerosol generating material:
The filter-tip rod is in a vertical state, wherein the aerosol generating matrix accommodating cavity (5) is vertically upward, and the flowing aerosol generating material is filled into the aerosol generating matrix accommodating cavity (5);Step 3, forming of an aerosol generating rod (6):
Rotate the filter-tip rod filled with aerosol generating material by 180° , so that the aerosol generating matrix accommodating cavity (5) is vertically downward, place it on the plane to dry and expand at a certain temperature, so that the aerosol generating material is solidified to form a fixed aerosol generating rod (6) in the aerosol generating matrix accommodating cavity (5). - The preparation method of claim 1, wherein, in step 1, the filter-tip rod can be cut into a plurality of filter tips, and the plurality of filter tips are connected by the filtering part (4) and or the aerosol generating matrix accommodating cavity (5).
At this time, there is also a cutting step between step 1 and step 2, which is to cut at the connected filtering part (4) and / or the connected aerosol generating matrix accommodating cavity (5), to cut the filter-tip rod into a plurality of filter tips. - The preparation method of claim 1, wherein, in step 2, the flowing aerosol generating material comprises smoking raw materials, smoking agents and solvents, the smoking raw materials are crushed in advance and passed through a 40-200 mesh sieve, the smoking raw materials after sieving are mixed separately with smoking agents and solvents in a certain proportion to form a flowing aerosol generating material.
The filling amount of the flowing aerosol generating material is 50-95 % of volume of the aerosol generating matrix accommodating cavity (5). - The preparation method of claim 3, wherein, in step 2, there is a binder in the flowing aerosol generating material, the flowing aerosol generating material is bonded to the inner wall of the composite tube (1) with its own binder during drying and expansion.
- The preparation method of claim 1, wherein, in step 2, the flowing aerosol generating material is squeezed into the aerosol generating matrix accommodating cavity (5) while cleaving to the inner surface of the composite tube (1), and the squeezed flowing aerosol generating material forms a central cavity; or,
The flowing aerosol generating material is filled into the aerosol generating matrix accommodating cavity (5) in two parts, wherein, a first part of the aerosol generating material is squeezed into the aerosol generating matrix accommodating cavity (5) while cleaving to the inner surface of the composite tube (1), the first part of the squeezed aerosol generating material forms a central cavity, and a second part of the aerosol generating material is squeezed into the central cavity, there is a gap between the first part of the aerosol generating material and the second part of the aerosol generating material. - The preparation method of claim 1, wherein, after step 2, there is also a sealing step to make the aerosol generating matrix accommodating cavity (5) filled with the aerosol generating matrix (6) far away from the end surface of the filtering section to form a sealing film.
- The preparation method of claim 1, wherein, drying temperature in step 3 depends on the solvent in the aerosol generating material, i.e., in case the solvent is ethanol, the drying temperature is 50-60°C, with drying time of 0.5-1h; in case the solvent is water, the drying temperature is 60-70°C, with the drying time of 1-2h.
- The method of claim 1, wherein, the cavity section (3) also comprises functional materials; and / or,
The cavity section (3) also comprises an empty-tube fitting. - The method of claim 1, wherein, the composite tube (1) in the cavity section (3) has an air vent (31) that penetrates radially through the composite tube (1).
- The preparation method of claim 1, wherein, there is a binder between the outer surface of the plugging part (2) and the inner surface of the composite tube (1), and there is a binder between the outer surface of the filtering part (4) and the inner surface of the composite tube (1).
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210707595.9A CN115039910B (en) | 2022-06-21 | 2022-06-21 | A kind of preparation method of multi-stage aerosol generating product |
| PCT/CN2022/100622 WO2023245528A1 (en) | 2022-06-21 | 2022-06-23 | Preparation method for multi-section aerosol generating product |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP4327672A1 EP4327672A1 (en) | 2024-02-28 |
| EP4327672A4 EP4327672A4 (en) | 2024-07-24 |
| EP4327672B1 true EP4327672B1 (en) | 2025-04-09 |
Family
ID=83162521
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP22865875.3A Active EP4327672B1 (en) | 2022-06-21 | 2022-06-23 | Preparation method for multi-section aerosol generating product |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP4327672B1 (en) |
| CN (1) | CN115039910B (en) |
| WO (1) | WO2023245528A1 (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN120206771A (en) * | 2023-12-27 | 2025-06-27 | 思摩尔国际控股有限公司 | A method and device for manufacturing an aerosol-generating substrate |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AR106163A1 (en) * | 2015-09-30 | 2017-12-20 | Philip Morris Products Sa | AEROSOL GENERATOR ITEM THAT HAS A SCATTERED FLAVOR |
| CN113925200B (en) * | 2016-03-09 | 2024-10-29 | 菲利普莫里斯生产公司 | Aerosol-generating article |
| EP3772248B1 (en) * | 2018-04-10 | 2026-05-06 | Philip Morris Products S.A. | An aerosol-generating article comprising a heatable element |
| KR102458829B1 (en) * | 2018-09-12 | 2022-10-26 | 주식회사 케이티앤지 | An aerosol generating rod comprising a capsule filter segment consisting of a hard capsule |
| CN109527638B (en) * | 2018-12-06 | 2023-08-08 | 安徽中烟工业有限责任公司 | Tobacco particle type heat-not-burn tobacco product and manufacturing method thereof |
| JP7373389B2 (en) * | 2018-12-20 | 2023-11-02 | フィリップ・モーリス・プロダクツ・ソシエテ・アノニム | Aerosol-generating articles with light hollow segments |
| CN119745125A (en) * | 2019-10-11 | 2025-04-04 | 科巴特(深圳)生活科技有限公司 | Heat-not-burn smoke-generating body |
| CN111567876A (en) * | 2020-05-06 | 2020-08-25 | 李可夫 | Aerosol generator having novel structure |
| CN111802698A (en) * | 2020-07-20 | 2020-10-23 | 云南喜科科技有限公司 | Method for filling aerosol generating products and aerosol generating products prepared |
| CN112716031B (en) * | 2021-01-08 | 2022-11-18 | 江西中烟工业有限责任公司 | Particle type aerosol generating product and rolling and forming method thereof |
| CN113925196B (en) * | 2021-11-30 | 2025-03-14 | 云南中烟工业有限责任公司 | An aerosol generating product with a segmented aerosol generating matrix rod |
-
2022
- 2022-06-21 CN CN202210707595.9A patent/CN115039910B/en active Active
- 2022-06-23 WO PCT/CN2022/100622 patent/WO2023245528A1/en not_active Ceased
- 2022-06-23 EP EP22865875.3A patent/EP4327672B1/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| EP4327672A1 (en) | 2024-02-28 |
| EP4327672A4 (en) | 2024-07-24 |
| WO2023245528A1 (en) | 2023-12-28 |
| CN115039910B (en) | 2023-02-24 |
| CN115039910A (en) | 2022-09-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN113925196B (en) | An aerosol generating product with a segmented aerosol generating matrix rod | |
| EP4327675B1 (en) | Aerosol generating product having composite-form blocking member | |
| CN113925197B (en) | An aerosol generating product having a particle-type aerosol generating matrix rod with high porosity | |
| CN114287665B (en) | A high-porosity aerosol generating matrix rod and an aerosol generating product containing the same | |
| CN114886158A (en) | Aerosol generating product with variable-diameter airflow channel plugging piece | |
| CN113940448B (en) | Intermittent spray type method for preparing segmented aerosol generating substrate rod | |
| EP4327672A1 (en) | Preparation method for multi-section aerosol generating product | |
| CN115413817A (en) | An aerosol generating article having a plug in the form of a porous aerosol generating matrix rod | |
| CN116326813B (en) | Tobacco rod type aerosol generating product and preparation method thereof | |
| CN115211585A (en) | Porous aerosol-generating matrix rod with channel structure, preparation method thereof, and aerosol-generating article comprising the same | |
| CN116584693A (en) | An aerosol-generating article in hollow form | |
| CN217065366U (en) | Aerosol-generating article with segmented aerosol-generating substrate rod | |
| CN114868960B (en) | An aerosol generating product with a multi-layer grooved corrugated structure | |
| CN114916700A (en) | Aroma-releasing and cooling composite material for heating non-combustible cigarettes as well as preparation method and application of composite material | |
| CN116210947B (en) | Preparation method of a falling tobacco stick type aerosol generating product | |
| CN116420909A (en) | A composite paper material and an aerosol-generating product containing it | |
| CN112841702B (en) | Heat-not-burn tobacco stick and preparation method thereof | |
| CN115039927A (en) | Preparation method of multi-section aerosol generating product with cavity structure | |
| CN221887692U (en) | A composite aerosol generating product of an empty pipe and a filter | |
| CN115606843A (en) | Aerosol generating product and manufacturing method and application thereof | |
| EP4193852B1 (en) | Double-layered heating cigarette, and preparation method therefor and use thereof | |
| CN104905401B (en) | A method for preparing cigarettes from smoke beads | |
| CN216906795U (en) | Aerosol-generating article having a particulate aerosol-generating substrate rod with high porosity | |
| CN114287666B (en) | A mixed high-porosity aerosol generating matrix rod and preparation method thereof | |
| CN116420908A (en) | Composite paper material with adsorption layer arranged in different regions and aerosol generating product containing same |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: UNKNOWN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20230313 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20240625 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: A24D 3/04 20060101ALI20240619BHEP Ipc: A24D 3/02 20060101ALI20240619BHEP Ipc: A24D 1/20 20200101ALI20240619BHEP Ipc: A24C 5/01 20200101ALI20240619BHEP Ipc: A24D 1/02 20060101ALI20240619BHEP Ipc: A24F 40/20 20200101AFI20240619BHEP |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: A24B 15/16 20200101ALI20241023BHEP Ipc: A24D 3/04 20060101ALI20241023BHEP Ipc: A24D 3/02 20060101ALI20241023BHEP Ipc: A24D 1/20 20200101ALI20241023BHEP Ipc: A24C 5/01 20200101ALI20241023BHEP Ipc: A24D 1/02 20060101ALI20241023BHEP Ipc: A24F 40/20 20200101AFI20241023BHEP |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| INTG | Intention to grant announced |
Effective date: 20241104 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Free format text: CASE NUMBER: APP_7992/2025 Effective date: 20250217 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602022013061 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20250721 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20250409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1782675 Country of ref document: AT Kind code of ref document: T Effective date: 20250409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250811 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250710 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250709 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250630 Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250709 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250809 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602022013061 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: H13 Free format text: ST27 STATUS EVENT CODE: U-0-0-H10-H13 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260127 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250623 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: L10 Free format text: ST27 STATUS EVENT CODE: U-0-0-L10-L00 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260218 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20250630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250409 |
|
| 26N | No opposition filed |
Effective date: 20260112 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250623 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20260101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250630 |