EP3969628B1 - Kaltgewalzter martensitischer stahl und verfahren zu seiner herstellung - Google Patents
Kaltgewalzter martensitischer stahl und verfahren zu seiner herstellung Download PDFInfo
- Publication number
- EP3969628B1 EP3969628B1 EP20716219.9A EP20716219A EP3969628B1 EP 3969628 B1 EP3969628 B1 EP 3969628B1 EP 20716219 A EP20716219 A EP 20716219A EP 3969628 B1 EP3969628 B1 EP 3969628B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- steel sheet
- cold rolled
- anyone
- cooling
- temperature
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C47/00—Winding-up, coiling or winding-off metal wire, metal band or other flexible metal material characterised by features relevant to metal processing only
- B21C47/02—Winding-up or coiling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/18—Hardening; Quenching with or without subsequent tempering
- C21D1/19—Hardening; Quenching with or without subsequent tempering by interrupted quenching
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/26—Methods of annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/004—Heat treatment of ferrous alloys containing Cr and Ni
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/005—Heat treatment of ferrous alloys containing Mn
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/008—Heat treatment of ferrous alloys containing Si
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0221—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the working steps
- C21D8/0226—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0221—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the working steps
- C21D8/0236—Cold rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0247—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the heat treatment
- C21D8/0273—Final recrystallisation annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/041—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing involving a particular fabrication or treatment of ingot or slab
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/0421—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the working steps
- C21D8/0426—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/0421—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the working steps
- C21D8/0436—Cold rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/0447—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the heat treatment
- C21D8/0463—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the heat treatment following hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/0447—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the heat treatment
- C21D8/0473—Final recrystallisation annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
- C21D9/48—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals deep-drawing sheets
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/001—Ferrous alloys, e.g. steel alloys containing N
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/002—Ferrous alloys, e.g. steel alloys containing In, Mg, or other elements not provided for in one single group C22C38/001 - C22C38/60
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/06—Ferrous alloys, e.g. steel alloys containing aluminium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/42—Ferrous alloys, e.g. steel alloys containing chromium with nickel with copper
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/44—Ferrous alloys, e.g. steel alloys containing chromium with nickel with molybdenum or tungsten
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/46—Ferrous alloys, e.g. steel alloys containing chromium with nickel with vanadium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/48—Ferrous alloys, e.g. steel alloys containing chromium with nickel with niobium or tantalum
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/50—Ferrous alloys, e.g. steel alloys containing chromium with nickel with titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/54—Ferrous alloys, e.g. steel alloys containing chromium with nickel with boron
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/58—Ferrous alloys, e.g. steel alloys containing chromium with nickel with more than 1.5% by weight of manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/60—Ferrous alloys, e.g. steel alloys containing lead, selenium, tellurium, or antimony, or more than 0.04% by weight of sulfur
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/002—Bainite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/005—Ferrite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/008—Martensite
Definitions
- the present invention relates to a method of manufacturing of a cold rolled martensitic steel suitable for automotive industry and particularly to Martensitic steels having tensile strength 1280 MPa or more.
- Automotive parts are required to satisfy two inconsistent necessities, viz. ease of forming and strength but in recent years a third requirement of improvement in fuel consumption is also bestowed upon automobiles in view of global environment concerns.
- automotive parts must be made of material having high formability in order that to fit in the criteria of ease of fit in the intricate automobile assembly and at same time have to improve strength for vehicle crashworthiness and durability while reducing weight of vehicle to improve fuel efficiency.
- EP3395993 is a cold-rolled steel sheet manufactured by a cold-rolled steel sheet manufacturing method comprising a continuous annealing step, which has a composition comprising, in percentage by weight: C: 0.1-0.15%; Si: 0.2% or less (including 0%); Mn: 2.3-3.0%; P: 0.001-0.10%; S: 0.010% or less (including 0%); Sol.Al: 0.01-0.10%; N: 0.010% or less (excluding 0%); Cr: 0.3-0.9%; B: 0.0010-0.0030%; Ti: 0.01-0.03%; Nb:0.01-0.03%; the balance being Fe and other impurities, and satisfies following relational expression (1).
- the present invention provides a high yield ratio type high strength cold-rolled steel sheet and the manufacturing method thereof, in which microstructure comprises, in area percentage, at least 90% of martensite and tempered martensite; and 10% or less of ferrite and bainite, in which the fraction of the tempered martensite in the martensite and the tempered martensite is 90% or more, in area percentage, and the ratio (b/a) of the C + Mn concentration (a) in the martensite to the C + Mn concentration (b) in the ferrite and the bainite is 0.65 or more.
- the steel sheet of WO2017/065371 is manufactured through the steps of: rapidly heating a material steel sheet for 3 to 60 seconds to an Ac3 transformation point or higher and maintaining the material steel sheet, the material steel sheet containing 0.08 to 0.30 wt% of C, 0.01 to 2.0 wt% of Si, 0.30 to 3.0 wt% of Mn, 0.05 wt% or less of P and 0.05 wt% or less of S and the remainder being Fe and other unavoidable impurities; rapidly cooling the heated steel sheet to 100°C/s or higher with water or oil; and rapidly tempering to 500°C to A1 transformation point for 3 to 60 seconds including heating and maintaining time.
- the steel of WO2017/065371 not able to surpass the tensile strength of 1300 MPa and do not mention about hole expansion ratio even having a tempered martensite single phase structure.
- WO2010/036028 relates to a hot dip galvanized steel sheet and a manufacturing method thereof.
- the hot dip galvanize steel sheet includes a steel sheet including a martensitic structure as a matrix, and a hot dip galvanized layer formed on the steel sheet.
- the steel sheet includes C of 0.05 wt % to 0.30 wt %, Mn of 0.5 wt % to 3.5 wt %, Si of 0.1 wt % to 0.8 wt %, Al of 0.01 wt % to 1.5 wt %, Cr of 0.01 wt % to 1.5 wt %, Mo of 0.01 wt % to 1.5 wt %, Ti of 0.001 wt % to 0.10 wt %, N of 5 ppm to 120 ppm, B of 3 ppm to 80 ppm, an impurity, and the remainder of Fe.
- the steel of WO2010/036028 does not mentions hole expansion ratio.
- the purpose of the present invention is to solve these problems by making available cold-rolled martensitic steel sheets that simultaneously have:
- such steel can also have a good suitability for forming, for rolling with good weldability and coatability.
- Another object of the present invention is also to make available a method for the manufacturing of these sheets that is compatible with conventional industrial applications while being robust towards manufacturing parameters shifts.
- the chemical composition of the cold rolled martensitic steel comprises of the following elements: Carbon is present in the steel of present invention is between 0.1% and 0.2%. Carbon is an element necessary for increasing the strength of the Steel of present invention by producing a low-temperature transformation phases such as Martensite, Therefore, Carbon plays two pivotal roles, one is to increase the strength. But Carbon content less than 0.1% will not be able to impart the tensile strength to the steel of present invention. On the other hand, at a Carbon content exceeding 0.2%, the steel exhibits poor spot weldability which limits its application for the automotive parts. A preferable content for the present invention may be kept between 0.11% and 0.19% and more preferably between 0.12% and 0.18%.
- Manganese content of the steel of present invention is between 1.5 % and 2.5%. This element is gammagenous. Manganese provides solid solution strengthening and suppresses the ferritic transformation temperature and reduces ferritic transformation rate hence assist in the formation of martensite. An amount of at least 1.5% is required to impart strength as well as to assist the formation of Martensite. But when Manganese content is more than 2.5% it produces adverse effects such as it retards transformation of Austenite to Martensite during cooling after annealing. Manganese content of above 2.5% can get excessively segregated in the steel during solidification and homogeneity inside the material is impaired which can cause surface cracks during a hot working process. The preferred limit for the presence of Manganese is between 1.6% and 2.4% and more preferably between 1.6% and 2.2%.
- Silicon content of the steel of present invention is between 0.1% and 0.25%.
- Silicon is an element that contributes to increasing the strength by solid solution strengthening. Silicon is a constituent that can retard the precipitation of carbides during cooling after annealing, therefore, Silicon promotes formation of Martensite. But Silicon is also a ferrite former and also increases the Ac3 transformation point which will push the annealing temperature to higher temperature ranges that is why the content of Silicon is kept at a maximum of 0.25%.Silicon content above 0.25% can also temper embrittlement and in addition silicon also impairs the coatability.
- the preferred limit for the presence of Silicon is between 0.16% and 0.24% and more preferably between 0.18% and 0.23%.
- Chromium content of the composite coil of steel of present invention is between 0.1% and 1%. Chromium is an essential element that provide strength to the steel by solid solution strengthening and a minimum of 0.1% is required to impart the strength but when used above 1% impairs surface finish of steel. The preferred limit for the presence of Chromium is between 0.1% and 0.5%.
- the content of the Aluminum is between 0.01% and 1%.
- Aluminum removes Oxygen existing in molten steel to prevent Oxygen from forming a gas phase during solidification process.
- Aluminum also fixes Nitrogen in the steel to form Aluminum nitride to reduce the size of the grains.
- Higher content of Aluminum, above 1%, increases Ac3 point to a high temperature thereby lowering the productivity.
- the preferred limit for the presence of Aluminium is between 0.01% and 0.05%
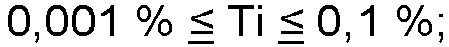
- Titanium is added to the Steel of present invention between 0.001 % to 0.1%. It forms Titanium-nitrides appearing during solidification of the cast product.
- the amount of Titanium is so limited to 0.1% to avoid the formation of coarse Titanium-nitrides detrimental for formability. In case the Titanium content below 0.001% does not impart any effect on the steel of present invention.
- Sulfur is not an essential element but may be contained as an impurity in steel and from point of view of the present invention the Sulfur content is preferably as low as possible but 0.09% or less from the viewpoint of manufacturing cost. Further if higher Sulfur is present in steel it combines to form Sulfides especially with Manganese and reduces its beneficial impact on the present invention.
- Phosphorus constituent of the Steel of present invention is between 0% and 0.09%, Phosphorus reduces the spot weldability and the hot ductility, particularly due to its tendency to segregate at the grain boundaries or co-segregate with Manganese. For these reasons, its content is limited to 0.09 % and preferably lower than 0.06%.
- Nitrogen is limited to 0.09% to avoid ageing of material and to minimize the precipitation of Aluminum nitrides during solidification which are detrimental for mechanical properties of the steel.
- Molybdenum is an optional element that constitutes 0% to 0.4% of the Steel of present invention; Molybdenum plays an effective role in improving hardenability and hardness, delays the appearance of Bainite hence promote the formation of Martensite, in particular when added in an amount of at least 0.001% or even of at least 0.002%. However, the addition of Molybdenum excessively increases the cost of the addition of alloy elements, so that for economic reasons its content is limited to 0.4%.
- Niobium is present in the Steel of present invention between 0% and 0.1% and suitable for forming carbo-nitrides to impart strength of the Steel of present invention by precipitation hardening. Niobium will also impact the size of microstructural components through its precipitation as carbo-nitrides and by retarding the recrystallization during heating process. Thus, finer microstructure formed at the end of the holding temperature and as a consequence after the complete annealing will lead to the hardening of the product. However, Niobium content above 0.1% is not economically interesting as a saturation effect of its influence is observed this means that additional amount of Niobium does not result in any strength improvement of the product.
- Vanadium is effective in enhancing the strength of steel by forming carbides or carbo-nitrides and the upper limit is 0.1% from economic points of view.
- Nickel may be added as an optional element in an amount of 0% to 1% to increase the strength of the steel present invention and to improve its toughness. A minimum of 0.01% is preferred to get such effects. However, when its content is above 1%, Nickel causes ductility deterioration.
- Copper may be added as an optional element in an amount of 0% to 1% to increase the strength of the of Steel of present invention and to improve its corrosion resistance. A minimum of 0.01% is preferred to get such effects. However, when its content is above 1%, it can degrade the surface aspects.
- Boron is an optional element for the steel of present invention and may be present between 0% and 0.05%. Boron forms boro-nitirides and impart additional strength to steel of present invention when added in an amount of at least 0.0001%.
- Calcium can be added to the steel of present invention in an among between 0.001% and 0.01%%. Calcium is added to steel of present invention as an optional element especially during the inclusion treatment. Calcium contributes towards the refining of the Steel by binding the detrimental Sulfur content in globular form thereby retarding the harmful effect of Sulfur.
- Sn , Pb or Sb can be added individually or in combination in the following proportions: Sn ⁇ 0.1%, Pb ⁇ 0.1% and Sb ⁇ 0.1%. Up to the maximum content levels indicated, these elements make it possible to refine the grain during solidification. The remainder of the composition of the steel consists of iron and inevitable impurities resulting from processing.
- Martensite constitutes at least 95% of the microstructure by area fraction.
- the martensite of the present invention can comprise both fresh and tempered martensite.
- fresh martensite is an optional microconstituent which is limited in the steel at an amount of between 0% an 4%, preferably between 0 and 2% and even better equal to 0%.
- Fresh martensite may form during cooling after tempering. Tempered martensite is formed from the martensite which forms during the second step of cooling after annealing and particularly after below Ms temperature and more particularly between Ms-10°C and 20°C.Such martensite is then tempered during the holding at a tempering temperature Ttemper between 150°C and 300°C.
- the martensite of the present invention imparts ductility and strength to such steel.
- the content of martensite is between 96% and 99% and more preferably between 97% and 99%.
- the cumulated amount of ferrite and bainite represents between 1% and 5% of the microstructure.
- the cumulative presence of bainite and ferrite does not affect adversely to the present invention till 5% but above 5% the mechanical properties may get impacted adversely.
- the preferred limit for the cumulative presence ferrite and bainite is kept between 1% and 4% and more preferably between 1% and 3%.
- Bainite forms during the reheating before tempering.
- the steel of present invention contains 1 to 3% of bainite. Bainite can impart formability to the steel but when present in a too big amount, it may adversely impact the tensile strength of the steel.
- Ferrite may form during the first step of cooling after annealing but is not required as a microstructural constituent. Ferrite formation must be kept as low as possible and preferably less than 2% or even less than 1%.
- Residual Austenite is an optional microstructure that can be present between 0% and 2% in the steel.
- the microstructure of the cold rolled martensitic steel sheet is free from microstructural components such as pearlite and cementite.
- the steel according to the invention can be manufactured by any suitable methods. It is however preferable to use the method according to the invention that will be detailed, as a non-limitative example.
- Such preferred method consists in providing a semi-finished casting of steel with a chemical composition of the prime steel according to the invention.
- the casting can be done either into ingots or continuously in form of thin slabs or thin strips, i.e. with a thickness ranging from approximately 220mm for slabs up to several tens of millimeters for thin strip.
- a slab having the chemical composition according to the invention is manufactured by continuous casting wherein the slab optionally underwent a direct soft reduction during the continuous casting process to avoid central segregation and to ensure a ratio of local Carbon to nominal Carbon kept below 1.10.
- the slab provided by continuous casting process can be used directly at a high temperature after the continuous casting or may be first cooled to room temperature and then reheated for hot rolling.
- the temperature of the slab which is subjected to hot rolling, must be at least 1000° C and must be below 1280°C. In case the temperature of the slab is lower than 1280° C, excessive load is imposed on a rolling mill and, further, the temperature of the steel may decrease to a Ferrite transformation temperature during finishing rolling, whereby the steel will be rolled in a state in which transformed Ferrite contained in the structure. Therefore, the temperature of the slab must be high enough so that hot rolling should be completed in the temperature range of Ac3 to Ac3+100°C. Reheating at temperatures above 1280°C must be avoided because they are industrially expensive.
- the sheet obtained in this manner is then cooled at a cooling rate of at least 20°C/s to the coiling temperature which must be below 650°C.
- the cooling rate will be less than or equal to 200° C/s.
- the hot rolled steel sheet is then coiled at a coiling temperature below 650°C to avoid ovalization and preferably between 475°C and 625°C to avoid scale formation, with an even prefererred range for such coiling temperature between 500°C and 625°C.
- the coiled hot rolled steel sheet is then cooled down to room temperature before subjecting it to optional hot band annealing.
- the hot rolled steel sheet may be subjected to an optional scale removal step to remove the scale formed during the hot rolling before optional hot band annealing.
- the hot rolled sheet may then have subjected to an optional hot band annealing.
- such hot band annealing is performed at temperatures between 400°C and 750°C, preferably for at least 12 hours and not more than 96 hours, the temperature preferably remaining below 750°C to avoid transforming partially the hot-rolled microstructure and, therefore, possibly losing the microstructure homogeneity.
- an optional scale removal step of this hot rolled steel sheet may be performed through, for example, pickling of such sheet.
- This hot rolled steel sheet is then subjected to cold rolling to obtain a cold rolled steel sheet with a thickness reduction between 35 to 90%.
- the cold rolled steel sheet is held at Tsoak during 10 seconds to 500 seconds to ensure a complete recrystallization and full transformation to austenite of the strongly work hardened initial structure.
- the cold rolled steel sheet is then cooled in a two steps cooling process wherein the first step of cooling starts from Tsoak, the cold rolled steel sheet being cooled down, at a cooling rate CR1 between 15°C/s and 150°C/s, to a temperature T1 which is in a range between 650°C and 750°C.
- the cooling rate CR1 for such first step of cooling is between 20°C/s and 120°C/s.
- the preferred T1 temperature for such first step is between 660°C and 725°C.
- the cold rolled steel sheet is cooled down from T1 to a temperature T2 which is between Ms-10°C and 20°C, at a cooling rate CR2 of at least 50°C/s.
- the cooling rate CR2 for the second step of cooling is at least 100°C/s and more preferably at least 150°C/s.
- the preferred T2 temperature for such second step is between Ms-50°C and 20°C.
- the cold rolled steel sheet is reheated to a tempering temperature Ttemper between 150°C and 300°C with a heating rate of at least 1°C/s and preferably of at least 2°C/s and more of at least 10°C/s during 100 s and 600 s.
- the preferred temperature range for tempering is between 200°C and 300°C and the preferred duration for holding at Ttemper is between 200 s and 500 s.
- the cold rolled steel sheet is cooled down to room temperature to obtain a cold rolled martensitic steel.
- the cold rolled martensitic steel sheet of the present invention may optionally be coated with zinc or zinc alloys, or with aluminum or aluminum alloys to improve its corrosion resistance.
- Table 1 Steel sheets made of steels with different compositions are gathered in Table 1, where the steel sheets are produced according to process parameters as stipulated in Table 2, respectively. Thereafter Table 3 gathers the microstructures of the steel sheets obtained during the trials and table 4 gathers the result of evaluations of obtained properties.
- Table 3 exemplifies the results of the tests conducted in accordance with the standards on different microscopes such as Scanning Electron Microscope for determining the microstructures of both the inventive and reference steels in terms of area fraction.
- Table 4 The results of the various mechanical tests conducted in accordance to the standards are gathered.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Heat Treatment Of Sheet Steel (AREA)
- Heat Treatment Of Steel (AREA)
Claims (18)
- Kaltgewalztes Stahlblech, umfassend die folgenden Elemente, ausgedrückt in Gewichtsprozent:




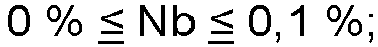
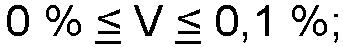


- Kaltgewalztes martensitisches Stahlblech nach Anspruch 1, wobei die Zusammensetzung 0,16 % bis 0,24 % Silizium beinhaltet.
- Kaltgewalztes martensitisches Stahlblech nach Anspruch 1 oder 2, wobei die Zusammensetzung 0,11 % bis 0,19 % Kohlenstoff beinhaltet.
- Kaltgewalztes martensitisches Stahlblech nach einem der Ansprüche 1 bis Anspruch 3, wobei die Zusammensetzung 0,01 % bis 0,05 % Aluminium beinhaltet.
- Kaltgewalztes martensitisches Stahlblech nach einem von Anspruch 1 bis 4, wobei die Zusammensetzung 1,6 % bis 2,4 % Mangan beinhaltet.
- Kaltgewalztes martensitisches Stahlblech nach einem der Ansprüche 1 bis 5, wobei die Zusammensetzung 0,1 % bis 0,5 % Chrom beinhaltet.
- Kaltgewalztes martensitisches Stahlblech nach einem der Ansprüche 1 bis 6, wobei die Menge an Martensit zwischen 96 % und 99 % ist.
- Kaltgewalztes martensitisches Stahlblech nach einem der Ansprüche 1 bis 7, wobei die kumulierte Menge an Ferrit und Bainit zwischen 1 % und 4 % ist.
- Kaltgewalztes martensitisches Stahlblech nach einem der Ansprüche 1 bis 8, wobei das Blech eine Zugfestigkeit von 1280 MPa oder mehr und eine Streckgrenze von 1100 MPa oder mehr aufweist.
- Verfahren zur Herstellung eines kaltgewalzten martensitisches Stahlblechs nach einem der Ansprüche 1 bis 9, umfassend die folgenden aufeinanderfolgenden Schritte:- Bereitstellen einer Zusammensetzung nach einem der Ansprüche 1 bis 6;- Wiedererhitzen des Halbfertigprodukts auf eine Temperatur zwischen 1000 °C und 1280 °C;- Walzen des Halbfertigprodukts in dem austenitischen Bereich, wobei die Warmwalzabschlusstemperatur zwischen Ac3 und Ac3 + 100 °C sein muss, um ein warmgewalztes Stahlblech zu erlangen;- Abkühlen des Blechs mit einer Abkühlgeschwindigkeit von mindestens 20 °C/s auf eine Aufwickeltemperatur, die unter 650 °C ist; und Aufwickeln des warmgewalzten Blechs;- Abkühlen des warmgewalzten Blechs auf Raumtemperatur;- optional Ausführen von Zunderentfernungsverfahren an dem warmgewalzten Stahlblech;- optional kann ein Glühen an warmgewalztem Stahlblech ausgeführt werden;- optional Ausführen eines Zunderentfernungsprozesses an dem warmgewalzten Stahlblech;- Kaltwalzen des warmgewalzten Stahlblechs mit einem Reduktionsgrad zwischen 35 und 90 %, um ein kaltgewalztes Stahlblech zu erlangen;- dann Erhitzen des kaltgewalzten Stahlblechs mit einer Geschwindigkeit von mindestens 2 °C/s auf eine Haltetemperatur Thalten zwischen Ac3 und Ac3+100 °C, wo es während 10 bis 500 Sekunden gehalten wird;- anschließend Abkühlen des kaltgewalzten Stahlblechs in einem zweistufigen Abkühlen, wobei:∘ die erste Stufe eines Abkühlens des kaltgewalzten Stahlblechs mit Thalten bis zu einer Temperatur T1 zwischen 650 °C und 750 °C, mit einer Abkühlgeschwindigkeit CR1 zwischen 15 °C/s und 150 °C/s beginnt;∘ die zweite Stufe eines Abkühlens bei T1 bis zu einer Temperatur T2 zwischen Ms-10 °C und 20 °C mit einer Abkühlgeschwindigkeit CR2 von mindestens 50 °C/s beginnt,- dann Wiedererhitzen des kaltgewalzten Stahlblechs mit einer Geschwindigkeit von mindestens 1 °C/s auf eine Anlasstemperatur Ttemper zwischen 150 °C und 300 °C, bei der es 100 bis 600 Sekunden gehalten wird;- dann Abkühlen auf Raumtemperatur mit einer Abkühlgeschwindigkeit von mindestens 1 °C/s, um ein kaltgewalztes martensitisches Stahlblech zu erlangen.
- Verfahren nach Anspruch 10, wobei die Aufwickeltemperatur zwischen 475 °C und 625 °C ist.
- Verfahren nach Anspruch 10 oder 11, wobei Thalten zwischen Ac3+10 °C und Ac3+100 °C ist.
- Verfahren nach einem der Ansprüche 10 bis 12, wobei CR1 zwischen 20 °C/s und 120 °C/s ist.
- Verfahren nach einem der Ansprüche 10 bis 13, wobei T1 zwischen 660 °C und 725 °C ist.
- Verfahren nach einem der Ansprüche 10 bis 14, wobei CR2 größer als 100 °C/s ist.
- Verfahren nach einem der Ansprüche 10 bis 15, wobei T2 zwischen Ms-50 °C und 20 °C ist.
- Verfahren nach einem der Ansprüche 10 bis 16, wobei Ttemper zwischen 200 °C und 300 °C ist.
- Verwendung eines Stahlblechs, das gemäß einem der Ansprüche 1 bis 9 erlangt werden kann, zum Herstellen eines Strukturteils eines Fahrzeugs.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/IB2019/054022 WO2020229877A1 (en) | 2019-05-15 | 2019-05-15 | A cold rolled martensitic steel and a method for it's manufacture |
| PCT/IB2020/052999 WO2020229898A1 (en) | 2019-05-15 | 2020-03-30 | A cold rolled martensitic steel and a method of martensitic steel thereof |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3969628A1 EP3969628A1 (de) | 2022-03-23 |
| EP3969628B1 true EP3969628B1 (de) | 2025-06-11 |
Family
ID=66630335
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20716219.9A Active EP3969628B1 (de) | 2019-05-15 | 2020-03-30 | Kaltgewalzter martensitischer stahl und verfahren zu seiner herstellung |
Country Status (14)
| Country | Link |
|---|---|
| US (1) | US20220213573A1 (de) |
| EP (1) | EP3969628B1 (de) |
| JP (2) | JP2022532625A (de) |
| KR (1) | KR102729387B1 (de) |
| CN (1) | CN113748219B (de) |
| CA (1) | CA3140117C (de) |
| ES (1) | ES3037769T3 (de) |
| FI (1) | FI3969628T3 (de) |
| HU (1) | HUE071952T2 (de) |
| MA (1) | MA55949A (de) |
| PL (1) | PL3969628T3 (de) |
| UA (1) | UA128744C2 (de) |
| WO (2) | WO2020229877A1 (de) |
| ZA (1) | ZA202107698B (de) |
Families Citing this family (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR102440757B1 (ko) * | 2020-12-03 | 2022-09-08 | 주식회사 포스코 | 굽힘가공성이 우수한 초고강도 냉연강판 및 그 제조방법 |
| EP4296394A4 (de) * | 2021-03-24 | 2024-07-24 | JFE Steel Corporation | Galvanisiertes stahlblech und kaltgewalztes stahlblech |
| CN113403535B (zh) * | 2021-05-31 | 2022-05-20 | 北京首钢股份有限公司 | 一种车厢板用热轧带钢及其制备方法 |
| JP2024524929A (ja) * | 2021-06-16 | 2024-07-09 | アルセロールミタル | 鋼部品の製造方法及び鋼部品 |
| CN114086071B (zh) * | 2021-11-19 | 2022-10-18 | 本钢板材股份有限公司 | 低成本1200Mpa级冷轧高强马氏体钢及其制造方法 |
| CN118974291A (zh) * | 2022-03-30 | 2024-11-15 | 杰富意钢铁株式会社 | 钢板和部件以及它们的制造方法 |
| JP7311070B1 (ja) * | 2022-03-30 | 2023-07-19 | Jfeスチール株式会社 | 鋼板および部材、ならびに、それらの製造方法 |
| WO2023188505A1 (ja) * | 2022-03-30 | 2023-10-05 | Jfeスチール株式会社 | 鋼板および部材、ならびに、それらの製造方法 |
| WO2023188504A1 (ja) * | 2022-03-30 | 2023-10-05 | Jfeスチール株式会社 | 鋼板および部材、ならびに、それらの製造方法 |
| KR20240172748A (ko) * | 2022-05-19 | 2024-12-10 | 아르셀러미탈 | 마르텐사이트계 강판 및 그 제조 방법 |
| CN115181908A (zh) * | 2022-07-07 | 2022-10-14 | 莱芜钢铁集团银山型钢有限公司 | 一种极寒地区服役特厚规格460MPa级钢板及其制备方法 |
| EP4569150A1 (de) * | 2022-08-12 | 2025-06-18 | ArcelorMittal | Kaltgewalzter martensitischer stahl und verfahren zu seiner herstellung |
| KR20240044568A (ko) * | 2022-09-28 | 2024-04-05 | 주식회사 포스코 | 우수한 강도 및 성형성을 갖는 냉연강판 및 그 제조방법 |
| WO2024105428A1 (en) * | 2022-11-14 | 2024-05-23 | Arcelormittal | High toughness press-hardened steel part and method of manufacturing the same |
| WO2024105429A1 (en) * | 2022-11-14 | 2024-05-23 | Arcelormittal | High toughness press-hardened steel part and method of manufacturing the same |
| KR20240098907A (ko) * | 2022-12-21 | 2024-06-28 | 주식회사 포스코 | 성형성 및 파괴저항성이 우수한 강판 및 그 제조방법 |
| KR20250059197A (ko) | 2023-10-24 | 2025-05-02 | (주)블루엔씨 | 스마트 센싱과 IoT 기능을 통한 바이스 클램프 모니터링 시스템 |
| CN117660836B (zh) * | 2023-11-30 | 2024-12-17 | 鞍钢股份有限公司 | 具有高延性的耐海洋大气腐蚀高强海工钢及其制造方法 |
| CN118835048A (zh) * | 2024-07-18 | 2024-10-25 | 首钢集团有限公司 | 一种热轧马氏体钢的制备方法、热轧马氏体钢 |
Family Cites Families (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH0925538A (ja) * | 1995-05-10 | 1997-01-28 | Kobe Steel Ltd | 耐孔明き腐食性および圧壊特性に優れた高強度冷延鋼板、および高強度亜鉛系めっき鋼板並びにそれらの製造方法 |
| JP3729108B2 (ja) | 2000-09-12 | 2005-12-21 | Jfeスチール株式会社 | 超高張力冷延鋼板およびその製造方法 |
| KR20100034118A (ko) | 2008-09-23 | 2010-04-01 | 포항공과대학교 산학협력단 | 마르텐사이트 조직을 가진 초고강도 용융아연도금 강판 및 그 제조 방법 |
| JP5136609B2 (ja) * | 2010-07-29 | 2013-02-06 | Jfeスチール株式会社 | 成形性および耐衝撃性に優れた高強度溶融亜鉛めっき鋼板およびその製造方法 |
| WO2013065346A1 (ja) * | 2011-11-01 | 2013-05-10 | Jfeスチール株式会社 | 曲げ特性と低温靭性に優れた高強度熱延鋼板およびその製造方法 |
| KR101467052B1 (ko) * | 2012-10-31 | 2014-12-10 | 현대제철 주식회사 | 초고강도 냉연강판 및 그 제조 방법 |
| JP5821912B2 (ja) * | 2013-08-09 | 2015-11-24 | Jfeスチール株式会社 | 高強度冷延鋼板およびその製造方法 |
| WO2015088523A1 (en) * | 2013-12-11 | 2015-06-18 | ArcelorMittal Investigación y Desarrollo, S.L. | Cold rolled and annealed steel sheet |
| KR101568549B1 (ko) * | 2013-12-25 | 2015-11-11 | 주식회사 포스코 | 우수한 굽힘성 및 초고강도를 갖는 열간 프레스 성형품용 강판, 이를 이용한 열간 프레스 성형품 및 이들의 제조방법 |
| BR112016018119B8 (pt) * | 2014-02-05 | 2020-12-15 | Arcelormittal S A | chapa de aço, método para produzir uma chapa de aço e uso de uma chapa de aço |
| EP3128026B1 (de) * | 2014-03-31 | 2019-03-06 | JFE Steel Corporation | Hochfestes kaltgewalztes stahlblech mit ausgezeichneter gleichmässigkeit der materialqualität und herstellungsverfahren dafür |
| WO2015177582A1 (fr) * | 2014-05-20 | 2015-11-26 | Arcelormittal Investigación Y Desarrollo Sl | Tôle d'acier doublement recuite à hautes caractéristiques mécaniques de résistance et ductilité, procédé de fabrication et utilisation de telles tôles |
| WO2017006144A1 (en) * | 2015-07-09 | 2017-01-12 | Arcelormittal | Steel for press hardening and press hardened part manufactured from such steel |
| KR101725274B1 (ko) | 2015-10-16 | 2017-04-10 | 삼화스틸(주) | 고강도 강판 및 그 제조방법 |
| KR101767780B1 (ko) * | 2015-12-23 | 2017-08-24 | 주식회사 포스코 | 고항복비형 고강도 냉연강판 및 그 제조방법 |
| WO2017125773A1 (en) * | 2016-01-18 | 2017-07-27 | Arcelormittal | High strength steel sheet having excellent formability and a method of manufacturing the same |
| CN107619993B (zh) * | 2016-07-13 | 2019-12-17 | 上海梅山钢铁股份有限公司 | 屈服强度750MPa级冷轧马氏体钢板及其制造方法 |
| JP6354919B1 (ja) * | 2016-08-30 | 2018-07-11 | Jfeスチール株式会社 | 薄鋼板およびその製造方法 |
| CA3233088A1 (en) * | 2021-10-29 | 2023-05-04 | Arcelormittal | Cold rolled and heat treated steel sheet and a method of manufacturing thereof |
-
2019
- 2019-05-15 WO PCT/IB2019/054022 patent/WO2020229877A1/en not_active Ceased
-
2020
- 2020-03-30 UA UAA202107252A patent/UA128744C2/uk unknown
- 2020-03-30 FI FIEP20716219.9T patent/FI3969628T3/fi active
- 2020-03-30 US US17/610,906 patent/US20220213573A1/en active Pending
- 2020-03-30 MA MA055949A patent/MA55949A/fr unknown
- 2020-03-30 HU HUE20716219A patent/HUE071952T2/hu unknown
- 2020-03-30 EP EP20716219.9A patent/EP3969628B1/de active Active
- 2020-03-30 CN CN202080031509.6A patent/CN113748219B/zh active Active
- 2020-03-30 KR KR1020217036177A patent/KR102729387B1/ko active Active
- 2020-03-30 PL PL20716219.9T patent/PL3969628T3/pl unknown
- 2020-03-30 JP JP2021568028A patent/JP2022532625A/ja active Pending
- 2020-03-30 ES ES20716219T patent/ES3037769T3/es active Active
- 2020-03-30 CA CA3140117A patent/CA3140117C/en active Active
- 2020-03-30 WO PCT/IB2020/052999 patent/WO2020229898A1/en not_active Ceased
-
2021
- 2021-10-12 ZA ZA2021/07698A patent/ZA202107698B/en unknown
-
2024
- 2024-01-25 JP JP2024009308A patent/JP7827756B2/ja active Active
Also Published As
| Publication number | Publication date |
|---|---|
| CN113748219A (zh) | 2021-12-03 |
| KR20210149145A (ko) | 2021-12-08 |
| ZA202107698B (en) | 2022-06-29 |
| MA55949A (fr) | 2022-03-23 |
| CA3140117A1 (en) | 2020-11-19 |
| PL3969628T3 (pl) | 2025-08-18 |
| JP2022532625A (ja) | 2022-07-15 |
| CA3140117C (en) | 2024-01-02 |
| ES3037769T3 (en) | 2025-10-07 |
| BR112021021486A2 (pt) | 2021-12-21 |
| US20220213573A1 (en) | 2022-07-07 |
| WO2020229898A1 (en) | 2020-11-19 |
| KR102729387B1 (ko) | 2024-11-14 |
| JP7827756B2 (ja) | 2026-03-10 |
| JP2024045307A (ja) | 2024-04-02 |
| CN113748219B (zh) | 2023-06-20 |
| HUE071952T2 (hu) | 2025-10-28 |
| UA128744C2 (uk) | 2024-10-09 |
| FI3969628T3 (fi) | 2025-07-31 |
| EP3969628A1 (de) | 2022-03-23 |
| WO2020229877A1 (en) | 2020-11-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA3140117C (en) | A cold rolled martensitic steel and a method of martensitic steel thereof | |
| EP3707289B1 (de) | Kaltgewalztes und wärmebehandeltes stahlblech und verfahren zu dessen herstellung | |
| EP3728679B1 (de) | Kaltgewalztes und wärmebehandeltes stahlblech und verfahren zu dessen herstellung | |
| CN113811624B (zh) | 经冷轧的马氏体钢及其马氏体钢的方法 | |
| EP3728668B1 (de) | Kaltgewalztes und beschichtetes stahlblech und verfahren zu seiner herstellung | |
| EP3856937B1 (de) | Warmgewalztes stahlblech und verfahren zu dessen herstellung | |
| EP3853387B1 (de) | Kaltgewalztes und beschichtetes stahlblech und verfahren zu seiner herstellung | |
| US12509740B2 (en) | Hot rolled and steel sheet and a method of manufacturing thereof | |
| EP4182488A1 (de) | Wärmebehandeltes kaltgewalztes stahlblech und verfahren zur herstellung davon | |
| WO2024033688A1 (en) | A cold rolled martensitic steel and method of producing thereof | |
| US12553099B2 (en) | Cold rolled and coated steel sheet and a method of manufacturing thereof | |
| WO2023223078A1 (en) | A martensitic steel sheet and a method of manunfacturing thereof | |
| CA3139633C (en) | A cold rolled martensitic steel and a method of martensitic steel thereof | |
| WO2025056941A1 (en) | A cold rolled martensitic steel and a method of martensitic steel thereof |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: UNKNOWN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20211013 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| RAV | Requested validation state of the european patent: fee paid |
Extension state: MA Effective date: 20211215 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20230403 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230522 |
|
| GRAJ | Information related to disapproval of communication of intention to grant by the applicant or resumption of examination proceedings by the epo deleted |
Free format text: ORIGINAL CODE: EPIDOSDIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17Q | First examination report despatched |
Effective date: 20230731 |
|
| INTC | Intention to grant announced (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20250207 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602020052594 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: FI Ref legal event code: FGE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 3037769 Country of ref document: ES Kind code of ref document: T3 Effective date: 20251007 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250911 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250912 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250611 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250611 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250911 |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E071952 Country of ref document: HU |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250611 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: T3 Ref document number: E 47034 Country of ref document: SK |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20251013 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20251011 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250611 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250611 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602020052594 Country of ref document: DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20260219 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20260219 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20260220 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250611 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20260219 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20260223 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20260219 Year of fee payment: 7 Ref country code: BE Payment date: 20260219 Year of fee payment: 7 Ref country code: RO Payment date: 20260303 Year of fee payment: 7 Ref country code: IT Payment date: 20260219 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: HU Payment date: 20260313 Year of fee payment: 7 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20260220 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20260227 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20260302 Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: L10 Free format text: ST27 STATUS EVENT CODE: U-0-0-L10-L00 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260423 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20260227 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SK Payment date: 20260226 Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: MA Ref legal event code: VAGR Ref document number: 55949 Country of ref document: MA Kind code of ref document: B1 |