EP3628831B1 - Tassenstössel mit rotationssicherung und verfahren zur herstellung - Google Patents
Tassenstössel mit rotationssicherung und verfahren zur herstellung Download PDFInfo
- Publication number
- EP3628831B1 EP3628831B1 EP19185122.9A EP19185122A EP3628831B1 EP 3628831 B1 EP3628831 B1 EP 3628831B1 EP 19185122 A EP19185122 A EP 19185122A EP 3628831 B1 EP3628831 B1 EP 3628831B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- wall
- bead
- tappet
- screw
- bore
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01L—CYCLICALLY OPERATING VALVES FOR MACHINES OR ENGINES
- F01L1/00—Valve-gear or valve arrangements, e.g. lift-valve gear
- F01L1/12—Transmitting gear between valve drive and valve
- F01L1/14—Tappets; Push rods
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21J—FORGING; HAMMERING; PRESSING METAL; RIVETING; FORGE FURNACES
- B21J5/00—Methods for forging, hammering, or pressing; Special equipment or accessories therefor
- B21J5/06—Methods for forging, hammering, or pressing; Special equipment or accessories therefor for performing particular operations
- B21J5/063—Friction heat forging
- B21J5/066—Flow drilling
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01L—CYCLICALLY OPERATING VALVES FOR MACHINES OR ENGINES
- F01L2303/00—Manufacturing of components used in valve arrangements
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F01—MACHINES OR ENGINES IN GENERAL; ENGINE PLANTS IN GENERAL; STEAM ENGINES
- F01L—CYCLICALLY OPERATING VALVES FOR MACHINES OR ENGINES
- F01L2307/00—Preventing the rotation of tappets
Definitions
- the present invention relates to a bucket tappet with a rotation lock, in particular a method for producing a bucket tappet with a rotation lock.
- Bucket tappets are used in the valve train, e.g. in combustion engines with an overhead camshaft, to transfer the force from the cams to the valves.
- no transmission element is necessary between the camshaft and valve, e.g. inlet or outlet valve.
- the cam lift is transmitted to the valve directly via the bottom of the bucket tappet.
- This direct drive is characterized by very high rigidity and at the same time small moving masses and is therefore particularly well suited for motors with high speeds. Friction losses occur at the contact surface between the cam and the cup base, the so-called sliding tap. However, these losses can be kept low through a suitable material pairing or friction-reducing coatings.
- the cam can be ground at an angle and attached laterally offset opposite the bucket tappet so that the bucket tappet is rotated by a certain angle around the valve axis, which runs in the actuating direction, with each actuation.
- the JP 2001 132413 A discloses a method for manufacturing a bucket tappet with rotation lock.
- the object of the present invention is therefore to provide a rotation lock for a bucket tappet that is easy to manufacture and allows short cycle times during manufacture. Another task is to provide a corresponding bucket tappet with a rotation lock.
- the method for producing the bucket tappet with rotation lock comprises providing a cup-shaped bucket tappet blank with a base and a cylindrical wall and flow drilling at least one hole in the wall so that an outer bead in the form of a web running around the at least one hole on an outside of the Wall is formed.
- the method can furthermore comprise removing an inner bead formed during flow drilling on an inner side of the wall.
- the flow drilling can be carried out such that an inner bead in the form of a web running around the at least one bore is formed on an inner side of the wall; and the method can further comprise introducing a thread into a through opening which is formed by the at least one bore, the associated outer bead and the associated inner bead.
- the method can comprise screwing a screw in the thread so that part of the screw protrudes outward beyond the outer bead.
- the screwing can take place from the outside, so that a screw head of the screw is arranged on the outside of the wall.
- the flow drilling can be carried out with a flow drill which has a collar with an annular recess.
- the flow drilling can include drilling a plurality of axially aligned bores.
- the bucket tappet with rotation lock comprises a base and a cylindrical wall, the wall having at least one bore and at least one outer bead in the form of a web surrounding the at least one bore being arranged on an outside of the wall.
- At least one inner bead in the form of a web surrounding the at least one bore can be arranged on an inner side of the wall, a through-opening formed by the at least one bore, the associated outer bead and the associated inner bead with is provided with a thread, and wherein a screw is screwed into the thread, wherein a part of the screw protrudes outwardly beyond the outer bead.
- a screw head of the screw can be arranged on the outside of the wall.
- the outer bead can have the shape of a hollow cylinder in an outer region.
- the wall can have multiple bores, the multiple bores being aligned with one another in the axial direction.
- a bucket tappet is specified which is produced using the method according to one of the above methods.
- FIGs 1A and 1B illustrate in a cross section the method according to the invention according to a first embodiment.
- a bucket tappet blank (see Fig. 1A ) is provided which has a cup shape (or bowl shape) with a base 2 and a cylindrical wall 4.
- 'Cylindrical wall' should be understood here to mean that the wall has the shape of a hollow cylinder.
- An axial direction, a radial direction and a circumferential direction are defined by the cylindrical shape of the wall 4.
- the bucket tappet blank is produced in a known manner, for example by deep drawing, forging or a machining process; a combination is also possible.
- the bucket tappet blank is preferably rotationally symmetrical.
- the bottom 2 and the wall 4 form a cavity which is open on a side opposite the bottom 2.
- This cavity defines an inside of the bucket tappet blank and the later bucket tappet, in particular also the wall 4; the sides of bottom 2 and wall 4 facing away from the cavity are defined as the outside; the terms 'outside' and 'inside' refer to this accordingly. (These definitions therefore agree with the usual notation for the inside and outside of a cup shape.)
- the material used for the cup tappet blank can be, for example, steel, a steel alloy, aluminum, brass or copper.
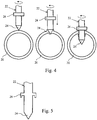
- a bore 6 is drilled into the wall 4 of the bucket tappet blank by means of flow drilling (see Fig. 4 and the associated description of the flow drilling process).
- This is done in such a way that an external bead 8 is formed at least on the outside of the wall 4 (see FIG Figure 1B ), which protrudes outwardly beyond the wall 4, the outer bead 8 thus forms a projection on the outside of the wall 4.
- an inner bead 10 will generally arise on the inside of the wall 4.
- Outer bead 8 and inner bead 10 have the shape of a web which runs around the bore 6.
- the flow drilling is preferably carried out from the outside. Flow drilling from the inside is also conceivable (if there is sufficient space).
- the projection formed by the outer bead 8 can engage or protrude into a groove provided on a bucket tappet guide (e.g. a guide bore in a cylinder head) in order to prevent the bucket tappet from rotating during operation.
- a bucket tappet guide e.g. a guide bore in a cylinder head
- the existing material of the wall 4 is used to prevent rotation form, further material and further work pieces (e.g. parts that are attached to the outside of the wall, e.g. by welding) are not necessary.
- the flow drilling process also runs relatively quickly (approx. 5 seconds), so that short cycle times are possible.
- an inner bead created during flow drilling can then be removed.
- a bucket tappet with rotation lock obtained in this way according to a second embodiment is shown in cross section in FIG Fig. 2 shown.
- the in Figure 1B any inner bead 10 that was still present was removed so that there is more space inside, for example for a valve holder. Otherwise, the same applies to the second embodiment in connection with the first embodiment ( Figures 1A, 1B )
- the outer bead 8 can continue to serve as a rotation lock by engaging in a corresponding groove.
- FIGS 3A and 3B a third embodiment is shown.
- a thread is introduced into the through-opening or socket formed by the bore 6, the outer bead 8 and the inner bead 10 (see Figure 3A ).
- the thread 12 is preferably introduced without cutting using a thread former.
- a screw 14 can be screwed into the thread 12, ie the screw 14 can be screwed into the thread 12 (see FIG Figure 3B ).
- the screw 14 is screwed in or screwed in such a way that part of the screw 14 protrudes outward beyond the outer bead 8 in order to serve as a rotation lock, ie this part of the screw 14 is provided to protrude into a corresponding groove. Because the thread 12 also extends over the outer bead 8 and the inner bead 10, there are enough threads to hold the screw 14 securely, although the wall 4 alone is generally not thick enough to accommodate a thread with a sufficient number To enable threads.
- the screwing can be done from the outside or the inside.
- a screw head 16 of the screw 14 comes to rest on the outside of the wall 4; the screw head 16 is then used to prevent rotation, which is provided in a engage the corresponding groove.
- an end of the screw 14 facing away from the screw head serves as a rotation lock; this end should remain free from a thread of the screw 14.
- a screw locking device can be provided, for example a screw locking adhesive.
- bores can also be made by flow drilling, each having an associated outer bead and / or inner bead.
- this description only describes one bore and associated features; what has been said in connection with a bore applies accordingly to each of the bores in the case of several bores.
- a hole ' is to be understood as' at least one hole'.
- each can be designed independently of one another in accordance with one of the embodiments described.
- several bores are axially aligned with one another.
- several bores are arranged opposite one another on the circumference of the wall. A combination of these two versions is also conceivable.
- a rotating flow drill 22 ie a flow drilling tool or flow drilling head, also referred to as a flow hole former
- the flow drill 22 has a conical tip 24 at one end of a cylindrical portion of the flow drill 22.
- the flow drill 22 has a collar 26 which is spaced from the conical tip 24 by at least the thickness of the wall 20 to be drilled through.
- the conical tip 24 of the flow drill 22 Since the conical tip 24 of the flow drill 22 is pressed against the wall 20 and rotates in the process Heat through friction, which leads to a heating of the material of the wall 20 at the drilling site and ultimately to a plasticization of the material. This enables a Penetration of the flow drill 22 into the wall 20, with the plasticized material being pressed aside with the formation of beads on both sides of the wall 20 (see middle part of the figure). Finally, after the conical tip 24 of the flow drill 22 has completely penetrated the wall 20, the flow drill 22 is advanced until the collar strikes the bead on the drill side and presses it flat (see right partial figure). By choosing the flow drilling process parameters, eg flow drill rotation speed, flow drill feed pressure, flow drill feed speed, the size of the inner bead or the outer bead can be controlled to a certain extent.
- the flow drilling process parameters eg flow drill rotation speed, flow drill feed pressure, flow drill feed speed, the size of the inner bead or the outer bead can be controlled to
- Fig. 5 shows in a cross section (for the sake of simplicity without hatching) a flow drill 22 preferably used for the method according to the invention.
- This has a collar 28 with an annular recess with a rectangular cross section running around the cylindrical part of the flow drill 22, which on the side of the Federal is located, which faces the conical tip 24; a rectangular cross-section of the recess is preferred, but it is also possible to deviate from this, for example to provide a trapezoidal cross-section.
- the annular recess begins (radially) on the inside, based on the flow drill, directly on the cylindrical part of the flow drill 22 and extends over a portion of the collar 28 (radially) outwards, based on the flow drill.
- the outer bead of the anti-rotation device in particular according to the first or second embodiment ( Fig. 1B, Fig. 2 ) to give a defined outer contour with a circular cylinder jacket surface, since the shape of the outer bead 8 formed is complementary to the shape of the recess on the collar 28. The dimensions there are therefore not dependent on the flow behavior of the material.
- the outer bead then has a defined radius in the areas that serve for guidance, so that the angular position of the bucket tappet relative to the cam can be determined by the groove in which the outer bead engages as a rotation lock (regardless of the flow behavior of the material conditional deviations).
- the outer bead has the shape of a hollow cylinder in an (radial, relative to the bucket tappet) outer region (ie at a free end of the bead).
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Valve-Gear Or Valve Arrangements (AREA)
Description
- Die vorliegende Erfindung betrifft einen Tassenstößel mit Rotationssicherung, insbesondere ein Verfahren zur Herstellung eines Tassenstößels mit Rotationssicherung.
- Tassenstößel kommen im Ventiltrieb, z.B. bei Verbrennungsmotoren mit obenliegender Nockenwelle, zum Einsatz, um die Kraft von den Nocken auf die Ventile zu übertragen. Beim Ventiltrieb mit Tassenstößel ist zwischen Nockenwelle und Ventil, z.B. Ein- bzw. Auslassventil, kein Übersetzungsglied notwendig. Der Nockenhub wird direkt über den Boden des Tassenstößels auf das Ventil übertragen. Dieser direkte Antrieb zeichnet sich durch sehr hohe Steifigkeit und gleichzeitig kleine bewegte Massen aus und ist dadurch besonders gut geeignet für Motoren mit hohen Drehzahlen. An der Kontaktfläche zwischen Nocken und Tassenboden, dem sogenannten Gleitabgriff, treten Reibungsverluste auf. Durch eine geeignete Werkstoffpaarung oder reibmindernde Beschichtungen können diese Verluste jedoch gering gehalten werden. Um den auftretenden Verschleiß weiter zu reduzieren, kann der Nocken schräg angeschliffen und dem Tassenstößel gegenüber seitlich versetzt angebracht sein, so dass der Tassenstößel bei jeder Betätigung um einen bestimmten Winkel um die Ventilachse, die in Betätigungsrichtung verläuft, gedreht wird.
- Bei Ausführungen von Tassenstößeln mit angepasster, z.B. zylindrischer, Nockenkontaktfläche, d.h. der Boden des Tassenstößels ist im Bereich der Kontaktfläche mit dem Nocken nicht eben sondern z.B. gewölbt, muss die Drehbewegung unterbunden werden, um die Vorteile der angepassten Nockenkontaktfläche auszunutzen. Eine Rotationssicherung hält dabei die Nockenkontaktfläche des Tassenstößels immer in der optimalen Winkelposition zum Nocken der Nockenwelle. Hierfür werden z.B. gesonderte Bauteile an der Außenseite des Tassenstößels befestigt. Die Herstellung solcher Rotationssicherungen ist kompliziert und zeitaufwendig.
- Die
JP 2001 132413 A - Aufgabe der vorliegenden Erfindung ist daher, eine Rotationssicherung für einen Tassenstößel bereitzustellen, die einfach herzustellen ist und kurze Taktzeiten bei der Herstellung erlaubt. Weiter ist es Aufgabe, einen entsprechenden Tassenstößel mit einer Rotationssicherung bereitzustellen.
- Die Aufgabe wird erfindungsgemäß gelöst durch ein Verfahren zur Herstellung eines Tassenstößels mit Rotationssicherung gemäß dem Anspruch 1 und durch einen Tassenstößel mit Rotationssicherung gemäß dem Anspruch 8. Abhängige Ansprüche betreffen bevorzugte Ausführungsformen.
- Das Verfahren zur Herstellung des Tassenstößels mit Rotationssicherung, umfasst Bereitstellen eines tassenförmigen Tassenstößel-Rohlings mit einem Boden und einer zylinderförmigen Wand und Fließbohren mindestens einer Bohrung in der Wand, so dass ein Außenwulst in Form eines um die mindestens eine Bohrung umlaufenden Steges an einer Außenseite der Wand gebildet wird.
- Gemäß einem weiteren Aspekt kann das Verfahren weiterhin Entfernen eines beim Fließbohren entstandenen Innenwulstes an einer Innenseite der Wand umfassen.
- Gemäß einem weiteren Aspekt kann das Fließbohren so ausgeführt werden, dass ein Innenwulst in Form eines um die mindestens eine Bohrung umlaufenden Steges an einer Innenseite der Wand gebildet wird; und kann das Verfahren weiterhin Einbringen eines Gewindes in eine Durchgangsöffnung, die durch die mindestens eine Bohrung, den zugehörigen Außenwulst und den zugehörigen Innenwulst gebildet wird, umfassen.
- Gemäß einem weiteren Aspekt kann das Verfahren Verschrauben einer Schraube in dem Gewinde, so dass ein Teil der Schraube über den Außenwulst nach außen hinausragt, umfassen.
- Gemäß einem weiteren Aspekt kann das Verschrauben von der Außenseite aus erfolgen, so dass ein Schraubenkopf der Schraube an der Außenseite der Wand angeordnet ist.
- Gemäß einem weiteren Aspekt kann das Fließbohren mit einem Fließbohrer ausgeführt werden, der einen Bund mit einer ringförmigen Aussparung aufweist.
- Gemäß einem weiteren Aspekt kann das Fließbohren das Bohren mehrerer axial miteinander ausgerichteter Bohrungen umfassen.
- Der Tassenstößel mit Rotationssicherung umfasst einen Boden und eine zylinderförmige Wand, wobei die Wand mindestens eine Bohrung aufweist und an einer Außenseite der Wand mindestens ein Außenwulst in Form eines um die mindestens eine Bohrung umlaufenden Steges angeordnet ist.
- Gemäß einem weiteren Aspekt des Tassenstößels kann an einer Innenseite der Wand mindestens ein Innenwulst in Form eines um die mindestens eine Bohrung umlaufenden Steges angeordnet sein, wobei eine Durchgangsöffnung, die durch die mindestens eine Bohrung, den zugehörigen Außenwulst und den zugehörigen Innenwulst gebildet ist, mit einem Gewinde versehen ist, und wobei eine Schraube in dem Gewinde verschraubt ist, wobei ein Teil der Schraube über den Außenwulst nach außen hinausragt.
- Gemäß einem weiteren Aspekt des Tassenstößels kann ein Schraubenkopf der Schraube an der Außenseite der Wand angeordnet sein.
- Gemäß einem weiteren Aspekt des Tassenstößels kann der Außenwulst in einem äußeren Bereich die Form eines Hohlzylinders aufweisen.
- Gemäß einem weiteren Aspekt des Tassenstößels kann die Wand mehrere Bohrungen aufweisen, wobei die mehreren Bohrungen miteinander in axialer Richtung ausgerichtet sind.
- Ferner ist angegeben ein Tassenstößel, der hergestellt ist mit dem Verfahren gemäß einem der vorstehenden Verfahren.
- Im Folgenden werden beispielhafte Ausführungsformen der Erfindung unter Bezug auf die Figuren genauer beschrieben, wobei
-
Fig. 1A einen Querschnitt eines Tassenstößel-Rohlings zeigt; -
Fig. 1B einen Querschnitt eines Tassenstößels mit einer durch Fließbohren hergestellten Rotationssicherung gemäß einer ersten Ausführungsform zeigt; -
Fig. 2 einen Querschnitt eines Tassenstößels mit einer durch Fließbohren hergestellten Rotationssicherung gemäß einer zweiten Ausführungsform zeigt; -
Fig. 3A und Fig. 3B weitere Herstellungsschritte und einen Tassenstößel mit Rotationssicherung gemäß einer dritten Ausführungsform im Querschnitt zeigen; -
Fig. 4 den Ablauf des Fließbohrens schematisch zeigt; und -
Fig. 5 einen Querschnitt eines bevorzugt verwendeten Fließbohrers zeigt. - In der Beschreibung und in der Zeichnung werden gleiche Bezugszeichen für gleiche oder ähnliche Elemente oder Komponenten verwendet. Es ist zudem eine Bezugszeichenliste angegeben, die für alle Figuren gültig ist. Die in den Figuren dargestellten Ausführungen sind lediglich schematisch und stellen nicht notwendigerweise die tatsächlichen Größenverhältnisse dar.
-
Fig. 1A und Fig. 1B illustrieren in einem Querschnitt das erfindungsgemäße Verfahren gemäß einer ersten Ausführungsform. Zunächst wird ein Tassenstößel-Rohling (sieheFig. 1A ) bereitgestellt, der eine Tassenform (bzw. Napfform) mit einem Boden 2 und einer zylinderförmigen Wand 4 aufweist. 'Zylinderförmige Wand' soll hier so zu verstehen sein, dass die Wand die Form eines Hohlzylinders aufweist. Durch die Zylinderform der Wand 4 werden eine axiale Richtung, eine radiale Richtung und eine Umfangsrichtung definiert. Der Tassenstößel-Rohling wird auf bekannte Weise hergestellt, beispielsweise durch Tiefzeihen, Schmieden oder ein spanendes Verfahren, auch eine Kombination ist möglich. Der Tassenstößel-Rohling ist bevorzugt rotationssymmetrisch. Durch den Boden 2 und die Wand 4 wird ein Hohlraum gebildet, der an einer dem Boden 2 gegenüberliegenden Seite offen ist. Dieser Hohlraum definiert eine Innenseite des Tassenstößel-Rohlings und des späteren Tassenstößels, insbesondere auch der Wand 4; als Außenseite sind entsprechend die vom Hohlraum abgewandten Seiten von Boden 2 und Wand 4 definiert; die Begriffe 'außen' und 'innen' beziehen sich entsprechend hierauf. (Diese Definitionen stimmen also mit der üblichen Bezeichnungsweise eines Inneren und Äußeren einer Tassenform überein.) Als Material für den Tassenstößel-Rohling kann z.B. Stahl, eine Stahllegierung, Aluminium, Messing oder Kupfer verwendet werden. - Anschließend wird in die Wand 4 des Tassenstößel-Rohlings eine Bohrung 6 mittels Fließbohren eingebracht (siehe
Fig. 4 und die zugehörige Beschreibung zum Ablauf des Fließbohrens). Dies erfolgt so, dass zumindest an der Außenseite der Wand 4 ein Außenwulst 8 gebildet wird (sieheFig. 1B ), der nach außen über die Wand 4 hinausragt, der Außenwulst 8 bildet also einen Vorsprung an der Außenseite der Wand 4. Ebenso wird im Allgemeinen ein Innenwulst 10 an der Innenseite der Wand 4 entstehen. Außenwulst 8 bzw. Innenwulst 10 weisen die Form eines Steges auf, der um die die Bohrung 6 verläuft. Bevorzugt erfolgt das Fließbohren von der Außenseite. Denkbar ist auch ein Fließbohren von der Innenseite (wenn ein ausreichender Raum vorhanden ist). - Der durch den Außenwulst 8 gebildete Vorsprung kann im eingebauten Zustand des Tassenstößels in eine dafür an einer Tassenstößel-Führung (z.B. einer Führungsbohrung in einem Zylinderkopf) vorgesehene Nut eingreifen bzw. in diese hineinragen, um so eine Rotation des Tassenstößels während des Betriebs zu verhindern. Beim Fließbohrvorgang wird das bereits vorhandene Material der Wand 4 dazu verwendet, die Rotationssicherung zu bilden, weiteres Material und weitere Werkstücke (z.B. Teile die außen an der Wand befestigt werden, etwa durch Schweißen) sind nicht notwendig. Auch läuft der Fließbohrvorgang relativ schnell ab (ca. 5 Sekunden), so dass kurze Taktzeiten möglich sind.
- Optional kann ein beim Fließbohren entstandener Innenwulst anschließend entfernt werden. Ein so erhaltener Tassenstößel mit Rotationssicherung gemäß einer zweiten Ausführungsform ist im Querschnitt in
Fig. 2 dargestellt. Der inFig. 1B noch vorhandene Innenwulst 10 wurde dabei entfernt, so dass im Inneren mehr Platz, z.B. für eine Ventilhalterung, vorhanden ist. Ansonsten gilt für die zweite Ausführungsform das im Zusammenhang mit der ersten Ausführungsform (Fig. 1A, Fig. 1B ) Gesagte, insbesondere kann der Außenwulst 8 weiterhin als Rotationssicherung dienen, indem er in eine korrespondierende Nut eingreift. - In
Fig. 3A und Fig. 3B ist eine dritte Ausführungsform dargestellt. Dabei wird nach dem Fließbohren der Bohrung 6 (also ausgehend von dem inFig. 1B dargestellten Zustand) ein Gewinde in die von der Bohrung 6, dem Außenwulst 8 und dem Innenwulst 10 gebildeten Durchgangsöffnung bzw. Buchse eingebracht (sieheFig. 3A ). Das Einbringen des Gewindes 12 erfolgt bevorzugt spanlos mit einem Gewindeformer. Nach dem Einbringen des Gewindes 12 kann eine Schraube 14 in das Gewinde 12 eingeschraubt werden, d.h. die Schraube 14 kann in dem Gewinde 12 verschraubt werden (sieheFig. 3B ). Das Einschrauben bzw. Verschrauben der Schraube 14 erfolgt so, dass ein Teil der Schraube 14 nach außen über den Außenwulst 8 hinausragt, um als Rotationssicherung zu dienen, d.h. dieser Teil der Schraube 14 ist vorgesehen, in eine entsprechende Nut hineinzuragen. Dadurch, dass sich das Gewinde 12 auch über den Außenwulst 8 und den Innenwulst 10 erstreckt, sind ausreichend viele Gewindegänge vorhanden, um die Schraube 14 sicher zu halten, obwohl die Wand 4 alleine im Allgemeinen nicht dick genug ist, um ein Gewinde mit ausreichend vielen Gewindegängen zu ermöglichen. - Das Verschrauben kann von der Außen- oder der Innenseite aus erfolgen. Im ersten Fall kommt ein Schraubenkopf 16 der Schraube 14 an der Außenseite der Wand 4 zum Liegen; der Schraubenkopf 16 dient dann also Rotationsicherung, die vorgesehen ist, in eine korrespondierende Nut einzugreifen. Falls das Verschrauben von der Innenseite erfolgt (nicht dargestellt), dient ein vom Schraubenkopf abgewandtes Ende der Schraube 14 als Rotationsicherung; dieses Ende sollte frei von einem Gewinde der Schraube 14 bleiben. Weiterhin können Mittel vorgesehen sein, die ein Lösen der Schraube während des Betriebs verhindern, d.h. es kann eine Schraubensicherung vorgesehen sein, z.B. ein Schraubensicherungskleber.
- Anstatt nur einer durch Fließbohren eingebrachten Bohrung und dem zugehörigen Außenwulst bzw. Innenwulst können auch mehrere Bohrungen durch Fließbohren eingebracht werden, die jeweils einen zugehörigen Außenwulst und/oder Innenwulst aufweisen. Zur sprachlichen Vereinfachung wird in dieser Beschreibung jeweils nur eine Bohrung und zugehörige Merkmale beschrieben, das im Zusammenhang mit einer Bohrung Gesagte gilt im Falle mehrerer Bohrungen entsprechend für jede der Bohrungen. Falls nichts anderes erwähnt ist, ist dementsprechend ,eine Bohrung' als 'mindestens eine Bohrung' zu verstehen. Im Falle mehrerer Bohrungen kann jede unabhängig voneinander entsprechend einer der verstehenden Ausführungsformen gestaltet sein. Weiterhin sind gemäß einer bevorzugten Ausführung mehrere Bohrungen axial miteinander ausgerichtet. Gemäß einer anderen Ausführung sind mehrere Bohrungen am Umfang der Wand gegenüberliegend angeordnet. Auch eine Kombination dieser beiden Ausführungen ist denkbar.
- In
Fig. 4 ist der Ablauf eines Fließbohrvorgangs in einem Querschnitt dargestellt (der Übersichtlichkeit halber wurde auf eine Schraffur verzichtet). Zunächst (siehe linke Teilfigur) wird ein rotierender Fließbohrer 22 (d.h. ein Fließbohrwerkzeug bzw. Fließbohrkopf, auch als Fließlochformer bezeichnet) auf eine hier zylinderförmige Wand 20, in die ein Loch gebohrt werden soll, aufgesetzt und gegen diese gedrückt. Der Fließbohrer 22 weist eine konische Spitze 24 an einem Ende eines zylindrischen Teils des Fließbohrers 22 auf. Weiterhin weist der Fließbohrer 22 einen Bund 26 auf, der von der konischen Spitze 24 beabstandet ist, und zwar mindestens um die Dicke der zu durchbohrenden Wand 20. Da die konische Spitze 24 des Fließbohrers 22 gegen die Wand 20 gedrückt wird und dabei rotiert, entsteht durch Reibung Wärme, die zu einer Erwärmung des Materials der Wand 20 an der Bohrstelle und letztendlich zu einer Plastifizierung des Materials führt. Dies ermöglicht ein Eindringen des Fließbohrers 22 in die Wand 20, wobei das plastifizierte Material unter Bildung von Wülsten auf beiden Seiten der Wand 20 beiseite gedrückt wird (siehe mittlere Teilfigur). Abschließend, nachdem die konische Spitze 24 des Fließbohrers 22 die Wand 20 vollständig durchdrungen hat, wird der Fließbohrer 22 so weit vorgeschoben, bis der Bund an den bohrerseitig gelegenen Wulst anschlägt und diesen flach drückt (siehe rechte Teilfigur). Durch Wahl der Fließbohr-Verfahrensparameter, z.B. Fließbohrer-Rotationsgeschwindigkeit, Fließbohrer-Vorschubdruck, Fließbohrer-Vorschubgeschwindigkeit, kann die Größe von Innenwulst bzw. Außenwulst in gewissem Umfang gesteuert werden. -
Fig. 5 stellt in einem Querschnitt (der Einfachheit halber ohne Schraffur) einen für das erfindungsgemäße Verfahren bevorzugt verwendeten Fließbohrers 22 dar. Dieser weist einen Bund 28 mit einer ringförmigen, um den zylindrischen Teil des Fließbohrers 22 verlaufenden Aussparung mit rechteckigem Querschnitt auf, die auf der Seite des Bundes gelegen ist, die der konischen Spitze 24 zugewandt ist; ein rechteckiger Querschnitt der Aussparung ist bevorzugt, es ist jedoch ebenso möglich davon abzuweichen, z.B. einen trapezförmigen Querschnitt vorzusehen. Die ringförmige Aussparung beginnt (radial) innen, bezogen auf den Fließbohrer, direkt am zylindrischen Teil des Fließbohrers 22 und erstreckt sich über einen Teilbereich des Bundes 28 (radial) nach außen, bezogen auf den Fließbohrer. Mit dem Einsatz eines solchen Fließbohrers 22 ist es möglich, dem Außenwulst der Rotationssicherung, insbesondere gemäß der ersten oder zweiten Ausführungsform (Fig. 1B, Fig. 2 ), eine definierte Außenkontur mit einer Kreiszylindermantelfläche zu geben, da die Form des gebildeten Außenwulsts 8 komplementär zur Form der Aussparung am Bund 28 ist. Die Abmessungen sind dort also nicht vom Fließverhalten des Materials abhängig. Der Außenwulst weist dann einen definierten Radius in den Bereichen, die zur Führung dienen, auf, so dass die Winkelposition des Tassenstößels relativ zum Nocken durch die Nut, in die der Außenwulst als Rotationssicherung eingreift, festgelegt werden kann (unabhängig von durch das Fließverhalten des Materials bedingten Abweichungen). Anders gesagt weist der Außenwulst gemäß dieser Ausführung in einem (radial, bezogen auf den Tassenstößel) äußeren Bereich (d.h. an einem freien Endes der Wulst) die Form eines Hohlzylinders auf. -
- 2
- Boden des Tassenstößels
- 4
- zylinderförmige Wand des Tassenstößels
- 6
- Bohrung
- 8
- Außenwulst
- 10
- Innenwulst
- 12
- Gewinde
- 14
- Schraube
- 16
- Schraubenkopf
- 20
- Wand
- 22
- Fließbohrer
- 24
- konische Spitze des Fließbohrers
- 26
- Bund des Fließbohrers
- 28
- Bund mit Aussparung
Claims (13)
- Verfahren zur Herstellung eines Tassenstößels mit Rotationssicherung, umfassend Bereitstellen eines tassenförmigen Tassenstößel-Rohlings mit einem Boden (2) und einer zylinderförmigen Wand (4); und
Fließbohren mindestens einer Bohrung (6) in der Wand (4), so dass ein Außenwulst (8) in Form eines um die mindestens eine Bohrung (6) umlaufenden Steges an einer Außenseite der Wand (4) gebildet wird. - Verfahren nach Anspruch 1, weiterhin umfassend
Entfernen eines beim Fließbohren entstandenen Innenwulstes (10) an einer Innenseite der Wand (4). - Verfahren nach Anspruch 1, wobei das Fließbohren so ausgeführt wird, dass ein Innenwulst (10) in Form eines um die mindestens eine Bohrung (6) umlaufenden Steges an einer Innenseite der Wand (4) gebildet wird; und weiterhin umfassend
Einbringen eines Gewindes (12) in eine Durchgangsöffnung, die durch die mindestens eine Bohrung (6), den zugehörigen Außenwulst (8) und den zugehörigen Innenwulst (10) gebildet wird. - Verfahren nach Anspruch 3, weiterhin umfassend
Verschrauben einer Schraube (14) in dem Gewinde (12), so dass ein Teil der Schraube (14) über den Außenwulst nach außen hinausragt. - Verfahren nach Anspruch 4, wobei das Verschrauben von der Außenseite aus erfolgt, so dass ein Schraubenkopf (16) der Schraube (14) an der Außenseite der Wand (4) angeordnet ist.
- Verfahren nach einem der vorstehenden Ansprüche, wobei das Fließbohren mit einem Fließbohrer (22) ausgeführt wird, der einen Bund (28) mit einer ringförmigen Aussparung aufweist.
- Verfahren nach einem der vorstehenden Ansprüche, wobei das Fließbohren das Bohren mehrerer axial miteinander ausgerichteter Bohrungen umfasst.
- Tassenstößel mit Rotationssicherung,
umfassend einen Boden (2) und eine zylinderförmige Wand (4), wobei die Wand (4) mindestens eine Bohrung (6) aufweist und an einer Außenseite der Wand (4) mindestens ein Außenwulst (8) in Form eines um die mindestens eine Bohrung (6) umlaufenden Steges angeordnet ist. - Tassenstößel nach Anspruch 8, wobei an einer Innenseite der Wand (4) mindestens ein Innenwulst (10) in Form eines um die mindestens eine Bohrung (6) umlaufenden Steges angeordnet ist, wobei eine Durchgangsöffnung, die durch die mindestens eine Bohrung (6), den zugehörigen Außenwulst (8) und den zugehörigen Innenwulst (10) gebildet ist, mit einem Gewinde (12) versehen ist, und wobei eine Schraube (14) in dem Gewinde (12) verschraubt ist, wobei ein Teil der Schraube (14) über den Außenwulst (8) nach außen hinausragt.
- Tassenstößel nach Anspruch 9, wobei ein Schraubenkopf (16) der Schraube (14) an der Außenseite der Wand (4) angeordnet ist.
- Tassenstößel nach einem der Ansprüche 8 - 10, wobei der Außenwulst (8) in einem äußeren Bereich die Form eines Hohlzylinders aufweist.
- Tassenstößel nach einem der Ansprüche 8 - 11, wobei die Wand (4) mehrere Bohrungen aufweist, wobei die mehreren Bohrungen miteinander in axialer Richtung ausgerichtet sind.
- Tassenstößel, hergestellt mit dem Verfahren gemäß einem der Ansprüche 1-7.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL19185122T PL3628831T3 (pl) | 2018-09-25 | 2019-07-09 | Popychacz szklankowy z zabezpieczeniem rotacyjnym i sposób wytwarzania |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102018123539.9A DE102018123539B3 (de) | 2018-09-25 | 2018-09-25 | Tassenstössel mit rotationssicherung und verfahren zur herstellung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3628831A1 EP3628831A1 (de) | 2020-04-01 |
| EP3628831B1 true EP3628831B1 (de) | 2021-01-13 |
Family
ID=67220681
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19185122.9A Active EP3628831B1 (de) | 2018-09-25 | 2019-07-09 | Tassenstössel mit rotationssicherung und verfahren zur herstellung |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP3628831B1 (de) |
| DE (1) | DE102018123539B3 (de) |
| PL (1) | PL3628831T3 (de) |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3429171A (en) * | 1965-10-21 | 1969-02-25 | Joseph J Feher | Radius spin drill |
| JP3700409B2 (ja) * | 1998-09-04 | 2005-09-28 | トヨタ自動車株式会社 | 3次元カム用バルブリフタおよび可変動弁装置 |
| JP2001132413A (ja) * | 1999-11-08 | 2001-05-15 | Toyota Motor Corp | 内燃機関用バルブリフタ及びその製造方法 |
| US20070170025A1 (en) * | 2006-01-25 | 2007-07-26 | Performance Automotive Group, Inc. | Dual cylinder shock and method therefor |
| JP5496696B2 (ja) * | 2010-01-27 | 2014-05-21 | Ntn株式会社 | ポンプ用タペット |
| LT6488B (lt) * | 2016-04-29 | 2018-01-25 | Kauno technologijos universitetas | Kombinuotas įrankis skylėms su sriegiu plonasienėse detalėse formuoti |
| FR3063923A1 (fr) * | 2017-03-16 | 2018-09-21 | Bollhoff Otalu S.A. | Procede d'assemblage d'un insert sur un support, et insert a assembler sur un support |
-
2018
- 2018-09-25 DE DE102018123539.9A patent/DE102018123539B3/de not_active Expired - Fee Related
-
2019
- 2019-07-09 EP EP19185122.9A patent/EP3628831B1/de active Active
- 2019-07-09 PL PL19185122T patent/PL3628831T3/pl unknown
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| PL3628831T3 (pl) | 2021-07-05 |
| DE102018123539B3 (de) | 2020-02-06 |
| EP3628831A1 (de) | 2020-04-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3487655B1 (de) | Fsw-werkzeug mit fester schulter | |
| EP2558230B1 (de) | Expansionskopf für aufweitwerkzeuge und diesen umfassendes expansionswerkzeug | |
| DE10136293A1 (de) | Gewindeformer oder -bohrer | |
| EP2888066B1 (de) | Einlippentieflochbohrer | |
| EP3639947B1 (de) | Verfahren und vorrichtung zur herstellung eines verbindungselementes | |
| EP3341617B1 (de) | Bohrschraube | |
| DE102016008767A1 (de) | Dehnspanneinrichtung | |
| DE102018123539B3 (de) | Tassenstössel mit rotationssicherung und verfahren zur herstellung | |
| EP3142819B1 (de) | Werkzeug zum aufrauen einer metallischen oberfläche und verfahren zum aufrauen einer mettalischen oberfläche mit einem solchen aufrauwerkzeug | |
| DE3334513A1 (de) | Verfahren zur herstellung von ventilhuelsen fuer drehschieberventile | |
| EP3738700B1 (de) | Hydraulisch spannbarer werkzeug-/werkstückhalter | |
| EP3085492B1 (de) | Schleifwerkzeug | |
| DE102007008142B4 (de) | Verfahren und Vorrichtungen zur Herstellung eines Mehrflächengleitlagers | |
| EP2174736A1 (de) | Hydraulische Dehnspanneinrichtung | |
| WO2014012821A1 (de) | Verfahren und komponenten zum herstellen einer werkzeugeinheit für eine tiefbohrmaschine | |
| DE202007019235U1 (de) | Stanzmutter | |
| WO2004020124A1 (de) | Verfahren zum herstellen einer spindelmutter eines kugelgewindetriebes | |
| DE10147581C1 (de) | Spannfutter | |
| DE102009040510A1 (de) | Rotor für eine Pumpe | |
| EP3988778B1 (de) | Kolben für eine brennkraftmaschine und herstellungsverfahren | |
| EP2876307B1 (de) | Arbeitszylinder und Verfahren zur Montage eines Arbeitszylinders | |
| EP3341156B1 (de) | Kolben einer brennkraftmaschine mit alkalimetallkühlung und verfahren zu seiner herstellung | |
| EP1877214B1 (de) | Drehverfahren | |
| DE102009007456B4 (de) | Verstellbare Reibahle | |
| DE10030614A1 (de) | Stanzstempel und Verfahren zu dessen Montage |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20200226 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20200824 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502019000682 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1354711 Country of ref document: AT Kind code of ref document: T Effective date: 20210215 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20210113 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210513 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210413 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210414 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210413 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210513 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502019000682 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| 26N | No opposition filed |
Effective date: 20211014 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20210731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210513 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210709 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210709 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210731 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210113 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230528 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20190709 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20230709 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230709 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210113 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20250620 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250620 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20250630 Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 1354711 Country of ref document: AT Kind code of ref document: T Effective date: 20240709 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250620 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250619 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240709 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20250630 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20260410 Year of fee payment: 5 |