EP2766503B2 - Verbessertes verfahren zum bearbeiten von metallblechen aus einer al-cu-li-legierung - Google Patents
Verbessertes verfahren zum bearbeiten von metallblechen aus einer al-cu-li-legierung Download PDFInfo
- Publication number
- EP2766503B2 EP2766503B2 EP12788613.3A EP12788613A EP2766503B2 EP 2766503 B2 EP2766503 B2 EP 2766503B2 EP 12788613 A EP12788613 A EP 12788613A EP 2766503 B2 EP2766503 B2 EP 2766503B2
- Authority
- EP
- European Patent Office
- Prior art keywords
- weight
- mpa
- heat treatment
- sheet
- short heat
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/12—Alloys based on aluminium with copper as the next major constituent
- C22C21/18—Alloys based on aluminium with copper as the next major constituent with zinc
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/12—Alloys based on aluminium with copper as the next major constituent
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/12—Alloys based on aluminium with copper as the next major constituent
- C22C21/14—Alloys based on aluminium with copper as the next major constituent with silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/12—Alloys based on aluminium with copper as the next major constituent
- C22C21/16—Alloys based on aluminium with copper as the next major constituent with magnesium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22F—CHANGING THE PHYSICAL STRUCTURE OF NON-FERROUS METALS AND NON-FERROUS ALLOYS
- C22F1/00—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working
- C22F1/002—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working by rapid cooling or quenching; cooling agents used therefor
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22F—CHANGING THE PHYSICAL STRUCTURE OF NON-FERROUS METALS AND NON-FERROUS ALLOYS
- C22F1/00—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working
- C22F1/04—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon
- C22F1/057—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon of alloys with copper as the next major constituent
Definitions
- the invention relates to products made of aluminum-copper-lithium alloys, more particularly, to such products, their methods of manufacture and use, intended in particular for aeronautical and aerospace construction.
- Lithium-containing aluminum alloys are very interesting in this respect, because lithium can reduce the density of aluminum by 3% and increase the modulus of elasticity by 6% for each percent by weight of lithium added.
- their performance relative to other use properties must reach that of commonly used alloys, particularly in terms of the trade-off between static strength properties (yield strength, fracture toughness) and damage tolerance properties (toughness, resistance to fatigue crack propagation), which are generally contradictory. Improving the trade-off between strength and damage tolerance is a constant pursuit.
- Al-Cu-Li alloy sheets are used in particular to manufacture aircraft fuselage elements or rocket elements that have a complex overall 3-dimensional shape.
- aircraft manufacturers seek to minimize the number of sheet forming steps, and to use sheets that can be manufactured inexpensively using short processing ranges, i.e. comprising as few individual steps as possible.
- a current practice of aircraft manufacturers generally consists of supplying hot-rolled or cold-rolled sheets according to the required thickness, in the as-manufactured state (state “F” according to the standard EN 515) in the quenched matured state (state “T3” or “T4"), or in the annealed state (state “O"), to subject them to a solution heat treatment followed by quenching, then to shape them on fresh quenching (state "W”), before finally subjecting them to natural or artificial ageing, so as to obtain the required mechanical characteristics.
- the sheets after solution treatment and quenching, the sheets are in a state characterized by good formability, but this state is unstable (state "W"), and the shaping must take place on fresh quenching, that is to say within a short time after quenching, of the order of a few tens of minutes to a few hours. If this is not possible for production management reasons, the sheet must be stored in a cold room at a sufficiently low temperature and for a sufficiently short period of time so as to avoid natural maturation. In some cases, it is found that for too short durations after solution treatment, Lüders lines appear after forming, which imposes an additional constraint with a minimum waiting time.
- this solution heat treatment requires large furnaces, which makes the operation inconvenient, even compared to the same operation carried out on flat sheet metal.
- the possible need for a cold room adds to the costs and disadvantages of the state of the art.
- the sheet metal can be deformed and pose problems related to this deformation, for example when it comes to positioning it in the jaws of the drawing-forming tool.
- this operation may have to be repeated if the material does not have, in its metallurgical state, sufficient formability to achieve the desired shape in a single operation.
- the patent US 5,455,003 describes a process for manufacturing Al-Cu-Li alloys which exhibit improved mechanical strength and toughness at cryogenic temperatures, in particular through appropriate work hardening and tempering.
- the patent US 7,229,509 describes an alloy comprising (wt%): (2.5-5.5) Cu, (0.1-2.5) Li, (0.2-1.0) Mg, (0.2-0.8) Ag, (0.2-0.8) Mn, 0.4 max Zr or other grain refining agents such as Cr, Ti, Hf, Sc, V.
- the patent application US 2009/142222 A1 describes alloys comprising (in wt %), 3.4 to 4.2% Cu, 0.9 to 1.4% Li, 0.3 to 0.7% Ag, 0.1 to 0.6% Mg, 0.2 to 0.8% Zn, 0.1 to 0.6% Mn and 0.01 to 0.6% of at least one element for controlling the grain structure. This application also describes a method of manufacturing extruded products.
- the patent EP 1,966,402 describes an alloy not containing zirconium intended for fuselage sheets of essentially recrystallized structure comprising (in % by weight) (2.1-2.8) Cu, (1.1-1.7) Li, (0.2-0.6) Mg, (0.1-0.8) Ag, (0.2-0.6) Mn.
- the products obtained in the T8 state are not suitable for forming, with in particular a ratio R m/ / R p0.2 less than 1.2 in the L and LT directions.
- the patent EP 1,891,247 describes an alloy for fuselage sheets comprising (in wt%) (3.0-3.4) Cu, (0.8-1.2) Li, (0.2-0.6) Mg, (0.2-0.5) Ag and at least one element from Zr, Mn, Cr, Sc, Hf and Ti, in which the Cu and Li contents meet the condition Cu + 5/3 Li ⁇ 5.2.
- the products obtained in the T8 state are not suitable for forming, with in particular a ratio R m/ / R p0.2 less than 1.2 in the L and LT directions. It has also been found that the overall energy at fracture measured by Kahn test which is related to toughness decreases with deformation and more abruptly for a deformation of 6%, which poses the problem of obtaining high toughness whatever the local deformation rate during forming.
- the patent EP 1045043 describes the manufacturing process for formed parts in AA2024 type alloy, and in particular for highly deformed parts, by combining an optimized chemical composition and specific manufacturing processes, making it possible to avoid as much as possible solution treatment on formed sheet metal.
- WO2006/131627 discloses a method of manufacturing an aluminum alloy-based sheet for the aerospace industry and suitable for use in fuselage applications, the sheet having superior toughness and mechanical strength high, in which: a) a liquid metal bath is prepared comprising 2.7 to 3.4% by weight of Cu, 0.8 to 1.4% by weight of Li, 0.1 to 0.8% by weight of weight of Ag, 0.2 to 0.6% by weight of Mg and at least one element selected from Zr, Mn, Cr, Sc, Hf and Ti, the amount of said element, if selected, being 0 ,05 to 0.13 wt% for Zr, 0.05 to 0.8 wt% for Mn, 0.05 to 0.3 wt% for Cr and for Sc, 0.05 to 0.5 wt% weight for Hf and 0.05 to 0.15 wt.% for Ti, the remainder being aluminium and unavoidable impurities, with the additional condition that the amount of Cu and Li is such that Cu (wt.%) ) + 5/3 Li (% by weight) ⁇ 5.2;
- a second subject of the invention is a rolled product obtainable by a process according to the invention, having between 0 and 50 days after short heat treatment, a combination of at least one property chosen from R p,2 (L) of at least 250 MPa, R p0,2 (LT) of at least 200 MPa and preferably at least 230 MPa, R m (L) of at least 380 MPa, R m (LT) of at least 320 MPa and preferably at least 360 MPa with a property chosen from A% (L) at least 15%, A% (LT) at least 24% and preferably at least 26%, R m /R p0,2 (L) at least 1.40 and preferably at least 1.45, R m /R p0,2 (LT) at least 1.45 and preferably at least 1.50.
- Another subject of the invention is a product capable of being obtained by a process according to the invention, having a tensile yield strength R p0.2 (L) at least substantially equal and a toughness K R greater, preferably by at least 5%, than those obtained by a similar process not comprising short heat treatment.
- Yet another object of the invention is the use of a product capable of being obtained by a process according to the invention for the manufacture of an aircraft fuselage skin.
- the plane stress toughness is determined by a stress intensity factor versus crack extension plot, known as the R-curve, according to ASTM E 561.
- the critical stress intensity factor K C in other words the stress intensity factor that makes the crack unstable, is calculated from the R-curve.
- the stress intensity factor K CO is also calculated by assigning the initial crack length to the critical load at the beginning of the monotonic loading. Both values are calculated for a specimen of the required shape.
- K app is the K CO factor corresponding to the specimen that was used to perform the R-curve test.
- K eff is the K C factor corresponding to the specimen that was used to perform the R-curve test.
- ⁇ a eff(max) is the crack extension of the last valid point on the R-curve.
- a "structural element” or “structural element” of a mechanical construction is a mechanical part for which the static and/or dynamic mechanical properties are particularly important for the performance of the structure, and for which a structural calculation is usually prescribed or carried out.
- These are typically elements whose failure is likely to endanger the safety of said construction, its users, its users or others.
- these structural elements include in particular the elements that make up the fuselage (such as the fuselage skin), the stringers, the bulkheads, the circumferential frames, the wings (such as the upper or lower wing skin, the stringers, the ribs and spars) and the empennage composed in particular of horizontal and vertical stabilisers, as well as the floor beams, the seat tracks and the doors.
- At least one short heat treatment is carried out with a duration and temperature such that the sheet reaches a temperature of between 130 and 170°C and preferably between 150 and 160°C for 0.1 to 13 hours, preferably 0.5 to 9 hours and more preferably 1 to 5 hours.
- the yield strength R p0.2 decreases by at least 20 MPa or even more, while the elongation A% is increased, i.e. it is multiplied by a factor of at least 1.1, or even at least 1.2 or even at least 1.3 compared to the state obtained without short heat treatment, typically T3 or T4.
- the short heat treatment is therefore not an income with which a T8 state would be obtained but a particular heat treatment which makes it possible to obtain a non-standardized state which is particularly suitable to the shaping.
- a sheet in the T8 state has a higher elastic limit than that of a T3 or T4 state whereas after the short heat treatment according to the invention the elastic limit is on the contrary lower than that of a T3 or T4 state.
- the short heat treatment is carried out so as to obtain a time equivalent to 150 °C of 0.5 h to 6 h and preferably of 1 h to 4 h and more preferably of 1 h to 3 h
- T (in Kelvin) is the instantaneous metal processing temperature, which changes with time t (in hours)
- T ref is a reference temperature set at 423 K.
- t i is expressed in hours
- the present inventors have found that the mechanical properties obtained after the short heat treatment are stable over time, which makes it possible to use the sheets in the state obtained after the short heat treatment instead of sheets in the O or W state for forming.
- the present inventors have found that, surprisingly, not only does the short heat treatment make it possible to simplify the manufacturing process of the products by eliminating the shaping in the O or W state, but also that the compromise between static mechanical strength and damage tolerance is at least identical or even improved thanks to the process of the invention, in the tempered state compared to a process not comprising a short heat treatment.
- the compromise obtained between static mechanical strength and toughness is improved compared to the state of the art.
- the advantage of the process according to the invention is obtained for products having a copper content of between 2.1 and 3.9% by weight.
- the copper content is at least 2.8% or 3% by weight.
- a maximum copper content of 3.7 or 3.5% by weight is preferred.
- the lithium content is between 0.7% or 0.8% and 2.0% by weight.
- the lithium content is at least 0.85% by weight.
- a maximum lithium content of 1.6 or even 1.2% by weight is preferred.
- the magnesium content is between 0.1% and 1.0% by weight. Preferably, the magnesium content is at least 0.2% or even 0.25% by weight. In one embodiment of the invention, the maximum magnesium content is 0.6% by weight.
- the silver content is between 0% and 0.6% by weight. In an advantageous embodiment of the invention, the silver content is between 0.1 and 0.5% by weight and preferably between 0.15 and 0.4% by weight. The addition of silver contributes to improving the compromise of mechanical properties of the products obtained by the process according to the invention.
- the zinc content is between 0% and 1% by weight.
- Zinc is generally an undesirable impurity, particularly due to its contribution to the density of the alloy, however in some cases zinc may be used alone or in combination with silver.
- the zinc content is less than 0.40 % by weight, preferably less than 0.2% by weight In one embodiment of the invention the zinc content is less than 0.04% by weight.
- the zirconium content is at least equal to 0.11% by weight.
- the manganese content is between 0.2 and 0.4% by weight and the zirconium content is less than 0.04% by weight.
- the sum of the iron content and the silicon content is at most 0.20% by weight.
- the iron and silicon contents are each at most 0.08% by weight.
- the iron and silicon contents are at most 0.06% and 0.04% by weight, respectively.
- a controlled and limited iron and silicon content contributes to improving the compromise between mechanical strength and damage tolerance.
- the other elements have a content of at most 0.05% by weight each and 0.15% by weight in total, these are unavoidable impurities, the remainder is aluminum.
- the manufacturing method according to the invention comprises the steps of preparation, casting, homogenization, rolling, solution treatment, quenching, planing and/or traction and short heat treatment.
- a bath of liquid metal is prepared so as to obtain an aluminum alloy of composition according to the invention.
- the bath of liquid metal is then cast in the form of a rolling plate.
- the rolling plate is then homogenized so as to reach a temperature of between 450°C and 550° and preferably between 480°C and 530°C for a period of between 5 and 60 hours.
- the homogenization treatment can be carried out in one or more stages.
- the rolling plate is then hot rolled and optionally cold rolled into a sheet.
- the thickness of said sheet is between 0.5 and 15 mm and preferably between 1 and 8 mm.
- the product thus obtained is then put into solution typically by a heat treatment allowing a temperature of between 490 and 530°C to be reached for 15 min to 8 h, then quenched typically with water at room temperature or preferably cold water.
- a planishing and/or traction is carried out in a controlled manner on said sheet metal with a cumulative deformation of at least 0.5% and less than 3%.
- the deformation made during the planishing is not always known precisely but it is estimated at approximately 0.5%.
- the traction controlled is implemented with a permanent deformation of between 0.5 to 2.5% and preferably between 0.5 to 1.5%. The combination of controlled traction with a preferred permanent deformation and a short heat treatment makes it possible to achieve optimum results in terms of formability and mechanical properties, especially when additional forming and tempering are carried out.
- the sheet obtained by the method according to the invention preferably has, between 0 and 50 days and preferably between 0 and 200 days after short heat treatment, a combination of at least one property chosen from R p0.2 (L) of at least 250 MPa, R p0.2 (LT) of at least 200 MPa and preferably at least 230 MPa, R m (L) of at least 380 MPa, R m (LT) of at least 320 MPa and preferably at least 360 MPa with a property chosen from A% (L) at least 15%, A% (LT) at least 24% and preferably at least 26%, R m /R p0.2 (L) at least 1.40 and preferably at least 1.45, R m /R p0.2 (LT) at least 1.45 and preferably at least 1.50. minus 1.50.
- the sheet obtained by the process according to the invention has a ratio R m /R p0.2 in the LT direction of at least 1.52 or 1.53.
- the sheet obtained by the process according to the invention has an elastic limit R p0.2 (L) of less than 290 MPa and preferably less than 280 MPa and R p0.2 (LT) of less than 270 MPa and preferably less than 260 MPa.
- the sheet is therefore ready for additional cold deformation, in particular a 3-dimensional shaping operation.
- An advantage of the invention is that this additional deformation can locally or generally reach values of 6 to 8% or even up to 10%.
- a minimum cumulative deformation of 2% between said additional deformation and the cumulative deformation by planishing and/or controlled traction carried out before the short heat treatment is advantageous.
- the additional cold deformation is locally or generally at least 1%, preferably at least 4% and preferably at least 6%.
- an income is carried out in which the said sheet reaches a temperature between 130 and 170°C and preferably between 150 and 160°C for 5 to 100 hours and preferably from 10 to 70 hours.
- the income can be carried out in one or more stages.
- the cold deformation is carried out by one or more shaping processes such as drawing, drawing-forming, stamping, flow forming or bending. In an advantageous embodiment, this involves shaping in the three dimensions of space to obtain a part of complex shape, preferably by drawing-forming.
- the product obtained at the end of the short heat treatment can be shaped as a product in state O or a product in state W.
- the short heat treatment can be carried out at the sheet metal manufacturer and the shaping at the aeronautical structure manufacturer, directly on the delivered product.
- the method according to the invention makes it possible to carry out the 3-dimensional shaping of a sheet metal at the end of the short heat treatment without the sheet metal being in a T8 state, an O state or a W state before this 3-dimensional shaping.
- a rolling plate made of AA2198 alloy was homogenized and then hot rolled to a thickness of 4 mm.
- the sheets thus obtained were solution-treated for 30 min at 505 °C and then quenched in water.
- the sheets were then pulled in a controlled manner.
- the controlled traction was achieved with a permanent elongation of 2.2%.
- the sheets then underwent a short heat treatment of 2 hours at 150°C.
- a rolling plate made of AA2198 alloy was homogenized and then hot rolled to a thickness of 4 mm.
- the sheets thus obtained were solution-treated for 30 min at 505 °C and then quenched in water.
- the sheets then underwent a short heat treatment of 2 hours at 150°C.
- the sheets thus obtained then underwent additional cold deformation by controlled traction with a permanent elongation of 2.5%, 4% or 8%.
- the sheets did not present any prohibitive Lüders lines after deformation.
- the sheets were finally tempered for 12 hours at 155 °C to obtain a T8 state.
- a sheet underwent a controlled 2% traction directly after quenching followed by tempering for 14 hours at 155 °C to the T8 state, without any intermediate short heat treatment.
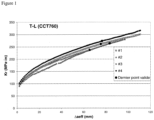
- the R curves were measured in the TL direction according to the E561-05 standard on CCT760 test specimens, which had a width of 760 mm.
- the obtained R curves are shown in the figure 1 .
- the sheets were then planed and tensioned in a controlled manner.
- the controlled tension was carried out with a permanent elongation of 1%.
- the sheets were aged sufficiently to reach a stabilized T3 state.
- the sheets were then subjected to a short heat treatment at 145 °C, 150 °C or 155 °C.
- the equivalent time at 150 °C was calculated taking into account a temperature rise rate of 20 °C/h.
- the static mechanical characteristics of the sheets were characterized after the short heat treatment in the TL direction.
- the R curves were measured according to E561-05 on CCT760 test specimens, which had a width of 760 mm in the T-L direction and in the L-T direction.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Metal Rolling (AREA)
- Heat Treatment Of Steel (AREA)
- Laminated Bodies (AREA)
Claims (16)
- Verfahren zur Herstellung eines Walzerzeugnisses aus Aluminiumlegierung insbesondere für die Luftfahrtindustrie, bei dem nacheinandera) ein Flüssigmetallbad auf Aluminiumbasis hergestellt wird, enthaltend 2,1 bis 3,9 Gew.-% Cu, 0,7 bis 2,0 Gew.-% Li, 0,1 bis 1,0 Gew.-% Mg, 0 bis 0,6 Gew.-% Ag, 0 bis 1 Gew.-% Zn, maximal 0,20 Gew.-% Fe + Si, wenigstens ein Element ausgewählt unter Zr, Mn, Cr, Sc, Hf und Ti, wobei die Menge des Elements, falls es gewählt wird, 0,05 bis 0,18 Gew.-% für Zr, 0,1 bis 0,6 Gew.-% für Mn, 0,05 bis 0,3 Gew.-% für Cr, 0,02 bis 0,2 Gew.-% für Sc, 0,05 bis 0,5 Gew.-% für Hf und 0,01 bis 0,15 Gew.-% für Ti beträgt, weitere Elemente jeweils maximal 0,05 Gew.-% und insgesamt 0,15 Gew.-%, Rest Aluminium;b) aus dem Flüssigmetallbad ein Walzbarren gegossen wird;c) der Walzbarren homogenisiert wird um eine Temperatur von 450°C bis 550°C während einer Zeitspanne von 5 bis 60 Stunden zu erreichen;d) der Walzbarren zu einem Blech warm- und wahlweise kaltgewalzt wird;e) das Blech lösungsgeglüht und abgeschreckt wird;f) das Blech gerichtet und/oder kontrolliert gezogen wird, mit einer Gesamtverformung von mindestens 0,5 % und weniger als 3,0 %,g) eine kurze Wärmebehandlung durchgeführt wird, bei der das Blech eine Temperatur zwischen 130 und 170°C und vorzugsweise zwischen 150 und 160°C während 0,1 bis 13 Stunden und vorzugsweise 1 bis 5 Stunden erreicht, wobei die kurze Wärmebehandlung eine Erniedrigung der Streckgrenze Rp0,2 um mindestens 20 MPa und eine Erhöhung der Dehnung A% induziert, so dass A% mindestens um einen Faktor 1,1 höher ist als in dem ohne kurze Wärmebehandlung erhaltenen Zustand.
- Verfahren nach Anspruch 1, bei dem die kurze Wärmebehandlung so durchgeführt wird, dass eine Äquivalentzeit bei 150°C von 0,5 bis 6 Stunden und vorzugsweise 1 Stunde bis 4 Stunden erhalten wird, wobei die Äquivalentzeit t i bei 150°C definiert ist durch die Formel

- Verfahren nach Anspruch 1 oder Anspruch 2, bei dem die Dicke des Blechs zwischen 0,5 und 15 mm und vorzugsweise zwischen 1 und 8 m beträgt.
- Verfahren nach irgendeinem der Ansprüche 1 bis 3, bei dem im Schritt f) ein kontrolliertes Ziehen mit einer bleibenden Verformung von 0,5 bis 1,5 % durchgeführt wird.
- Verfahren nach irgendeinem der Ansprüche 1 bis 4, bei dem der Kupfergehalt mindestens 3 und höchstens 3,5 Gew.-% beträgt.
- Verfahren nach irgendeinem der Ansprüche 1 bis 5, bei dem der Lithiumgehalt mindestens 0,85 und höchstens 1,2 Gew.-% beträgt.
- Verfahren nach irgendeinem der Ansprüche 1 bis 6, bei dem der Magnesiumgehalt mindestens 0,2 und höchstens 0,6 Gew.-% beträgt.
- Verfahren nach irgendeinem der Ansprüche 1 bis 7, bei dem der Silbergehalt zwischen 0,1 und 0,5 Gew.-% und vorzugsweise zwischen 0,15 und 0,4 Gew.-% beträgt und/oder der Zinkgehalt kleiner als 0,4 Gew.-% und vorzugsweise kleiner als 0,2 Gew.-% ist.
- Verfahren nach irgendeinem der Ansprüche 1 bis 8, bei dem die Legierung zwischen 0,08 und 0,15 Gew.-% Zirconium, zwischen 0,01 und 0,10 Gew.-% Titan enthält und bei dem der Gehalt an Mn, Cr, Sc und Hf höchstens 0,05 Gew.-% beträgt.
- Verfahren nach irgendeinem der Ansprüche 1 bis 9, bei dem nach dem Schritt g)h) eine weitere Kaltverformung des Blechs so durchgeführt wird, dass diese weitere Verformung weniger als 10 % beträgt,i) eine Auslagerungsbehandlung durchgeführt wird, bei der das Blech eine Temperatur zwischen 130 und 170°C und vorzugsweise zwischen 150 und 160°C während 5 bis 100 Stunden und vorzugsweise 10 bis 70 Stunden erreicht.
- Verfahren nach Anspruch 10, bei dem die weitere Kaltverformung örtlich oder allgemein mindestens 1 %, vorzugsweise mindestens 4 % und bevorzugt mindestens 6 % beträgt.
- Verfahren nach Anspruch 10 oder Anspruch 11, bei dem die Kaltverformung mittels einem oder mehreren Formgebungsverfahren durchgeführt wird, wie z.B. Ziehen, Ziehformen, Tiefziehen, Drückwalzen oder Biegen.
- Walzerzeugnis, erhältlich durch das Verfahren nach irgendeinem der Ansprüche 1 bis 9, das 0 bis 5 Tage nach der kurzen Wärmebehandlung eine Eigenschaftskombination aufweist, bestehend aus mindestens einer Eigenschaft ausgewählt unter Rp0,2(L) von mindestens 250 MPa, Rp0,2(LT) von mindestens 200 MPa und vorzugsweise mindestens 230 MPa, Rm(L) von mindestens 380 MPa, Rm(LT) von mindestens 320 MPa und vorzugsweise mindestens 360 MPa, und einer Eigenschaft ausgewählt unter A%(L) von mindestens 15%, A% (LT) von mindestens 24% und vorzugsweise mindestens 26%, Rm/Rp0,2(L) von mindestens 1,40 und vorzugsweise mindestens 1,45, Rm/Rp0,2(LT) von mindestens 1,45 und vorzugsweise mindestens 1,50.
- Walzerzeugnis, erhältlich durch das Verfahren nach irgendeinem der Ansprüche 10 bis 12, das eine zumindest im Wesentlichen gleiche Streckgrenze unter Zugbeanspruchung Rp0,2(L) und eine vorzugsweise um mindestens 5% höhere Zähigkeit im Vergleich zur Zähigkeit aufweist, die durch ein ähnliches Verfahren ohne kurze Wärmebehandlung erhalten wird.
- Walzerzeugnis, erhältlich durch das Verfahren nach irgendeinem der Ansprüche 10 bis 12, dadurch gekennzeichnet, dass es sich um ein Blech aus der Legierung AA2198 mit einer Dicke von 0,5 bis 15 mm und vorzugsweise 1 bis 8 mm handelt, das nach Warmauslagerung im Zustand T8 eine Eigenschaftskombination aufweist, bestehend aus mindestens einer statischen Festigkeitseigenschaft ausgewählt unter Rp0,2(L) von mindestens 500 MPa und vorzugsweise mindestens 510 MPa und/oder Rp0,2(LT) von mindestens 480 MPa und vorzugsweise mindestens 490 MPa, und mindestens einer, an Proben vom Typ CCT760 (mit 2ao = 253 mm) gemessenen Zähigkeitseigenschaft ausgewählt unter Kapp in TL-Richtung von mindestens 160 MPa√m und vorzugsweise mindestens 170 MPa√m und/oder Keff in TL-Richtung von mindestens 200 MPa√m und vorzugsweise mindestens 220 MPa√m und/oder Δeff(max) in TL-Richtung von mindestens 40 mm und vorzugsweise mindestens 50 mm.
- Verwendung eines durch das Verfahren nach irgendeinem der Ansprüche 10 bis 12 erhältlichen Walzerzeugnisses für die Herstellung eines Flugzeugstrukturelementes, insbesondere einer Rumpfhaut eines Flugzeugs.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE12788613.3T DE12788613T1 (de) | 2011-10-14 | 2012-10-12 | Verbessertes Verfahren zum Bearbeiten von Metallblechen aus einer AL-CU-LI-Legierung |
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US201161547289P | 2011-10-14 | 2011-10-14 | |
| FR1103155A FR2981365B1 (fr) | 2011-10-14 | 2011-10-14 | Procede de transformation ameliore de toles en alliage al-cu-li |
| PCT/FR2012/000414 WO2013054013A1 (fr) | 2011-10-14 | 2012-10-12 | Procédé de transformation amélioré de tôles en alliage al-cu-li |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP2766503A1 EP2766503A1 (de) | 2014-08-20 |
| EP2766503B1 EP2766503B1 (de) | 2016-12-07 |
| EP2766503B2 true EP2766503B2 (de) | 2024-09-11 |
Family
ID=45350826
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12788613.3A Active EP2766503B2 (de) | 2011-10-14 | 2012-10-12 | Verbessertes verfahren zum bearbeiten von metallblechen aus einer al-cu-li-legierung |
Country Status (8)
| Country | Link |
|---|---|
| US (2) | US10968501B2 (de) |
| EP (1) | EP2766503B2 (de) |
| CN (2) | CN106222504B (de) |
| BR (1) | BR112014008685B1 (de) |
| CA (1) | CA2851592C (de) |
| DE (1) | DE12788613T1 (de) |
| FR (1) | FR2981365B1 (de) |
| WO (1) | WO2013054013A1 (de) |
Families Citing this family (32)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR3004197B1 (fr) | 2013-04-03 | 2015-03-27 | Constellium France | Toles minces en alliage d'aluminium-cuivre-lithium pour la fabrication de fuselages d'avion. |
| CN103484738A (zh) * | 2013-08-12 | 2014-01-01 | 安徽盛达前亮铝业有限公司 | 一种高耐损伤铝合金板材的生产工艺 |
| FR3014448B1 (fr) * | 2013-12-05 | 2016-04-15 | Constellium France | Produit en alliage aluminium-cuivre-lithium pour element d'intrados a proprietes ameliorees |
| RU2560481C1 (ru) * | 2014-07-01 | 2015-08-20 | Федеральное государственное унитарное предприятие "Всероссийский научно-исследовательский институт авиационных материалов" (ФГУП "ВИАМ") | СПЛАВ НА ОСНОВЕ СИСТЕМЫ Al-Cu-Li И ИЗДЕЛИЕ, ВЫПОЛНЕННОЕ ИЗ НЕГО |
| FR3026747B1 (fr) * | 2014-10-03 | 2016-11-04 | Constellium France | Toles isotropes en alliage d'aluminium-cuivre-lithium pour la fabrication de fuselages d'avion |
| US10253404B2 (en) * | 2014-10-26 | 2019-04-09 | Kaiser Aluminum Fabricated Products, Llc | High strength, high formability, and low cost aluminum-lithium alloys |
| US9419580B2 (en) | 2014-10-31 | 2016-08-16 | Raytheon Company | Output matching network having a single combined series and shunt capacitor component |
| WO2017060697A1 (en) * | 2015-10-06 | 2017-04-13 | Bae Systems Plc | Metal object production |
| EP3153600A1 (de) * | 2015-10-06 | 2017-04-12 | BAE Systems PLC | Metallobjektherstellung |
| EP3153601A1 (de) * | 2015-10-06 | 2017-04-12 | BAE Systems PLC | Metallobjektherstellung |
| FR3044682B1 (fr) * | 2015-12-04 | 2018-01-12 | Constellium Issoire | Alliage aluminium cuivre lithium a resistance mecanique et tenacite ameliorees |
| CA3032261A1 (en) | 2016-08-26 | 2018-03-01 | Shape Corp. | Warm forming process and apparatus for transverse bending of an extruded aluminum beam to warm form a vehicle structural component |
| CN106244874B (zh) * | 2016-08-27 | 2019-05-07 | 来安县科来兴实业有限责任公司 | 一种高速动车组齿轮箱箱体专用耐热铝合金及其制备方法 |
| FR3057476B1 (fr) | 2016-10-17 | 2018-10-12 | Constellium Issoire | Toles minces en alliage aluminium-magnesium-scandium pour applications aerospatiales |
| CN110114498A (zh) | 2016-10-24 | 2019-08-09 | 形状集团 | 用于生产车辆零件的多阶段铝合金形成与热加工方法 |
| FR3065012B1 (fr) * | 2017-04-10 | 2022-03-18 | Constellium Issoire | Produits en alliage aluminium-cuivre-lithium a faible densite |
| FR3067620B1 (fr) * | 2017-06-19 | 2019-08-02 | Constellium Issoire | Toles minces en alliage d'aluminium-cuivre-lithium pour la fabrication de fuselage d'avion |
| FR3075078B1 (fr) | 2017-12-20 | 2020-11-13 | Constellium Issoire | Procede de fabrication ameliore de toles en alliage d'aluminium-cuivre-lithium pour la fabrication de fuselage d'avion |
| US20190233921A1 (en) * | 2018-02-01 | 2019-08-01 | Kaiser Aluminum Fabricated Products, Llc | Low Cost, Low Density, Substantially Ag-Free and Zn-Free Aluminum-Lithium Plate Alloy for Aerospace Application |
| FR3080861B1 (fr) * | 2018-05-02 | 2021-03-19 | Constellium Issoire | Procede de fabrication d'un alliage aluminium cuivre lithium a resistance en compression et tenacite ameliorees |
| CN108823519B (zh) * | 2018-07-02 | 2021-10-01 | 鼎镁新材料科技股份有限公司 | 一种高Mg含量中强高延变形铝锂合金及其热处理方法 |
| CN108754263A (zh) * | 2018-07-30 | 2018-11-06 | 东北轻合金有限责任公司 | 一种高强度航天用铝锂合金型材及其制备方法 |
| FR3087206B1 (fr) * | 2018-10-10 | 2022-02-11 | Constellium Issoire | Tôle en alliage 2XXX à haute performance pour fuselage d’avion |
| CN110423926B (zh) * | 2019-07-29 | 2020-12-29 | 中国航发北京航空材料研究院 | 一种耐热铝锂合金及其制备方法 |
| CN110512125B (zh) * | 2019-08-30 | 2020-09-22 | 中国航发北京航空材料研究院 | 一种用于增材制造的直径铝锂合金丝材的制备方法 |
| CN110791720B (zh) * | 2019-11-25 | 2020-11-24 | 重庆文理学院 | 一种抑制铝锂合金再结晶的加工方法 |
| FR3104172B1 (fr) * | 2019-12-06 | 2022-04-29 | Constellium Issoire | Tôles minces en alliage d’aluminium-cuivre-lithium à ténacité améliorée et procédé de fabrication |
| US12203159B2 (en) | 2021-04-23 | 2025-01-21 | Universal Alloy Corporation | Method for producing aluminum-copper alloys containing scandium |
| FR3132306B1 (fr) | 2022-01-28 | 2024-05-03 | Constellium Issoire | Tôle mince améliorée en alliage d’aluminium-cuivre-lithium |
| CN114622108A (zh) * | 2022-02-10 | 2022-06-14 | 山东南山铝业股份有限公司 | 一种绿色循环保级6系高强度汽车板生产方法 |
| CN119061301A (zh) * | 2024-11-05 | 2024-12-03 | 湖南大学苏州研究院 | 一种用于塑性成形的低成本高强韧铝合金铸坯及其制备方法 |
| CN120311083B (zh) * | 2025-04-23 | 2026-01-16 | 有研工程技术研究院有限公司 | 一种轻质超高强高模量可焊铝锂合金材料及其制备方法 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20080289728A1 (en) † | 2005-06-06 | 2008-11-27 | Bernard Bes | High fracture toughness aluminum-copper-lithium sheet or light-gauge plate suitable for use in a fuselage panel |
| WO2012033949A2 (en) † | 2010-09-08 | 2012-03-15 | Alcoa Inc. | Improved aluminum-lithium alloys, and methods for producing the same |
Family Cites Families (25)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2083576A (en) * | 1935-09-20 | 1937-06-15 | Aluminum Co Of America | Heat treatment of aluminum alloys |
| US3706606A (en) * | 1970-02-10 | 1972-12-19 | L Esercizio Dell Inst Sperimen | Thermomechanical treatment process for heat treatable aluminium alloys |
| US3947297A (en) * | 1973-04-18 | 1976-03-30 | The United States Of America As Represented By The Secretary Of The Air Force | Treatment of aluminum alloys |
| US5116572A (en) * | 1983-12-30 | 1992-05-26 | The Boeing Company | Aluminum-lithium alloy |
| US4806174A (en) * | 1984-03-29 | 1989-02-21 | Aluminum Company Of America | Aluminum-lithium alloys and method of making the same |
| US4648913A (en) * | 1984-03-29 | 1987-03-10 | Aluminum Company Of America | Aluminum-lithium alloys and method |
| US4812178A (en) * | 1986-12-05 | 1989-03-14 | Bruno Dubost | Method of heat treatment of Al-based alloys containing Li and the product obtained by the method |
| US5032359A (en) | 1987-08-10 | 1991-07-16 | Martin Marietta Corporation | Ultra high strength weldable aluminum-lithium alloys |
| US5066342A (en) * | 1988-01-28 | 1991-11-19 | Aluminum Company Of America | Aluminum-lithium alloys and method of making the same |
| US4869870A (en) * | 1988-03-24 | 1989-09-26 | Aluminum Company Of America | Aluminum-lithium alloys with hafnium |
| US5259897A (en) * | 1988-08-18 | 1993-11-09 | Martin Marietta Corporation | Ultrahigh strength Al-Cu-Li-Mg alloys |
| US5455003A (en) | 1988-08-18 | 1995-10-03 | Martin Marietta Corporation | Al-Cu-Li alloys with improved cryogenic fracture toughness |
| US5076859A (en) * | 1989-12-26 | 1991-12-31 | Aluminum Company Of America | Heat treatment of aluminum-lithium alloys |
| US5234662A (en) * | 1991-02-15 | 1993-08-10 | Reynolds Metals Company | Low density aluminum lithium alloy |
| US7438772B2 (en) * | 1998-06-24 | 2008-10-21 | Alcoa Inc. | Aluminum-copper-magnesium alloys having ancillary additions of lithium |
| FR2792001B1 (fr) * | 1999-04-12 | 2001-05-18 | Pechiney Rhenalu | Procede de fabrication de pieces de forme en alliage d'aluminium type 2024 |
| EP1409759A4 (de) * | 2000-10-20 | 2004-05-06 | Pechiney Rolled Products Llc | Hochfeste aluminiumlegierung |
| EP1641953A4 (de) * | 2003-05-28 | 2007-08-01 | Alcan Rolled Products Ravenswood Llc | Neue al-cu-li-mg-ag-mn-zr-legierung für bauanwendungen, die hohe festigkeit und hohe bruchzähigkeit erfordern |
| DE602006003656D1 (de) * | 2005-06-06 | 2008-12-24 | Alcan Rhenalu | Hochfestes aluminium-kupfer-lithium-blech für flugzeugrümpfe |
| US8771441B2 (en) * | 2005-12-20 | 2014-07-08 | Bernard Bes | High fracture toughness aluminum-copper-lithium sheet or light-gauge plates suitable for fuselage panels |
| FR2894985B1 (fr) | 2005-12-20 | 2008-01-18 | Alcan Rhenalu Sa | Tole en aluminium-cuivre-lithium a haute tenacite pour fuselage d'avion |
| US8118950B2 (en) * | 2007-12-04 | 2012-02-21 | Alcoa Inc. | Aluminum-copper-lithium alloys |
| FR2945464B1 (fr) * | 2009-05-13 | 2012-03-23 | Alcan Rhenalu | Procede d'assemblage par soudage de pieces en alliage d'aluminium. |
| FR2947282B1 (fr) * | 2009-06-25 | 2011-08-05 | Alcan Rhenalu | Alliage aluminium cuivre lithium a resistance mecanique et tenacite ameliorees |
| CN101967588B (zh) * | 2010-10-27 | 2012-08-29 | 中国航空工业集团公司北京航空材料研究院 | 一种耐损伤铝锂合金及其制备方法 |
-
2011
- 2011-10-14 FR FR1103155A patent/FR2981365B1/fr active Active
-
2012
- 2012-10-12 CA CA2851592A patent/CA2851592C/fr active Active
- 2012-10-12 CN CN201610576196.8A patent/CN106222504B/zh active Active
- 2012-10-12 EP EP12788613.3A patent/EP2766503B2/de active Active
- 2012-10-12 BR BR112014008685-0A patent/BR112014008685B1/pt active IP Right Grant
- 2012-10-12 CN CN201280050425.2A patent/CN103874775B/zh active Active
- 2012-10-12 DE DE12788613.3T patent/DE12788613T1/de active Pending
- 2012-10-12 WO PCT/FR2012/000414 patent/WO2013054013A1/fr not_active Ceased
- 2012-10-12 US US13/651,002 patent/US10968501B2/en active Active
-
2018
- 2018-11-08 US US16/184,046 patent/US11667994B2/en active Active
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20080289728A1 (en) † | 2005-06-06 | 2008-11-27 | Bernard Bes | High fracture toughness aluminum-copper-lithium sheet or light-gauge plate suitable for use in a fuselage panel |
| WO2012033949A2 (en) † | 2010-09-08 | 2012-03-15 | Alcoa Inc. | Improved aluminum-lithium alloys, and methods for producing the same |
Non-Patent Citations (1)
| Title |
|---|
| B. DECREUS ET AL.: "Understanding the mechanical properties of 2198 Al-Li-Cu alloy in relation with the intra-granular and inter- granular precipitate microstructure", 15TH INTERNATIONAL CONFERENCE ON THE STRENGTH OF MATERIALS (ICSMA 15), JOURNAL OF PHYSICS: CONFERENCE SERIES, vol. 240, no. 1, 2010, pages 012096 † |
Also Published As
| Publication number | Publication date |
|---|---|
| DE12788613T1 (de) | 2015-02-19 |
| EP2766503B1 (de) | 2016-12-07 |
| EP2766503A1 (de) | 2014-08-20 |
| CA2851592A1 (fr) | 2013-04-18 |
| CN106222504A (zh) | 2016-12-14 |
| CN106222504B (zh) | 2019-10-18 |
| US10968501B2 (en) | 2021-04-06 |
| BR112014008685B1 (pt) | 2019-04-24 |
| BR112014008685A2 (pt) | 2017-04-25 |
| CA2851592C (fr) | 2020-01-07 |
| CN103874775A (zh) | 2014-06-18 |
| FR2981365B1 (fr) | 2018-01-12 |
| FR2981365A1 (fr) | 2013-04-19 |
| US20190071753A1 (en) | 2019-03-07 |
| US11667994B2 (en) | 2023-06-06 |
| US20130092294A1 (en) | 2013-04-18 |
| CN103874775B (zh) | 2016-07-06 |
| WO2013054013A1 (fr) | 2013-04-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2766503B1 (de) | Verbessertes verfahren zum bearbeiten von metallblechen aus einer al-cu-li-legierung | |
| EP2984195B1 (de) | Verfahren zur umformung von blechen aus al-cu-li-legierung für verbesserte formbarkeit und korrosionsbeständigkeit | |
| EP2364378B1 (de) | Produkte aus aluminium-kupfer-lithium-legierung | |
| EP2449142B1 (de) | Aluminium-kupfer-lithium-legierung mit verbesserten mechanische beständigkeit und zähigkeit | |
| EP2655680B1 (de) | Aluminium-kupfer-lithium-legierung mit verbesserter druckfestigkeit und beständigkeit | |
| EP3384061B1 (de) | Aluminium-kupfer-lithium-legierung mit verbesserter mechanischer festigkeit und erhöhter zähigkeit | |
| EP3011068B1 (de) | Bogenrückenstrukturelement aus einer aluminium-kupfer-lithium-legierung | |
| EP1966402B1 (de) | Blech aus einer hochfesten aluminiumlegierung mit kupfer und lithium für einen flugzeugrumpf | |
| EP3526358B1 (de) | Dünne bleche aus aluminium-magnesium-scandium-legierung für anwendungen in der luft- und raumfahrt | |
| EP3201371B1 (de) | Verfahren zur herstellung eines knetproduktes aus einer aluminium-magnesium-lithium legierung, knetprodukt und vervendung des knetproduktes | |
| EP2981632B1 (de) | Dünne bleche aus einer aluminium-kupfer-lithium-legierung zur herstellung von flugzeugrümpfen | |
| FR2853666A1 (fr) | ALLIAGE Al-Zn A HAUTE RESISTANCE,PROCEDE DE PRODUCTION DE PRODUITS EN UN TEL ALLIAGE, ET PRODUITS OBTENUS SELON CE PROCEDE | |
| EP3201372B1 (de) | Isotropische bleche aus aluminium-lithium-kupfer legierung für die herstellung von flugzeugrümpfen und herstellungsverfahren davon | |
| FR2838135A1 (fr) | PRODUITS CORROYES EN ALLIAGES A1-Zn-Mg-Cu A TRES HAUTES CARACTERISTIQUES MECANIQUES, ET ELEMENTS DE STRUCTURE D'AERONEF | |
| EP3788178B1 (de) | Aluminium-kupfer-lithium-legierung mit verbesserter kompressionsfestigkeit und erhöhter beständigkeit | |
| EP3788179A1 (de) | Verfahren zur herstellung einer aluminium-kupfer-lithium-legierung mit verbesserter druckfestigkeit und verbesserter zähigkeit | |
| EP4069875A1 (de) | Dünnschichten aus aluminium-kupfer-lithium-legierung mit verbesserter zähigkeit und verfahren zur herstellung einer dünnschicht aus aluminium-kupfer-lithium-legierung | |
| EP3362584B1 (de) | Dünne bleche aus aluminium-magnesium-zirkonium-legierungen für luft- und raumfahrtanwendungen | |
| CA3037115C (fr) | Toles minces en alliage aluminium-magnesium-scandium pour applications aerospatiales |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20140508 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GBCC | Gb: corrected translation (of claims) filed (gb section 80(3)/1977) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R210 Ref document number: 602012026357 Country of ref document: DE Effective date: 20150219 Ref country code: DE Ref legal event code: R210 Effective date: 20150219 |
|
| 17Q | First examination report despatched |
Effective date: 20151222 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: CONSTELLIUM ISSOIRE |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAJ | Information related to disapproval of communication of intention to grant by the applicant or resumption of examination proceedings by the epo deleted |
Free format text: ORIGINAL CODE: EPIDOSDIGR1 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20160623 |
|
| INTG | Intention to grant announced |
Effective date: 20160705 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 602012026357 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: AT Ref legal event code: REF Ref document number: 851784 Country of ref document: AT Kind code of ref document: T Effective date: 20161215 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: FRENCH |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602012026357 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D Ref country code: NO Ref legal event code: T2 Effective date: 20161207 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20161207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170308 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 851784 Country of ref document: AT Kind code of ref document: T Effective date: 20161207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170407 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170307 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170407 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R026 Ref document number: 602012026357 Country of ref document: DE |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: ARCONIC INC. Effective date: 20170907 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171012 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171012 |
|
| APBM | Appeal reference recorded |
Free format text: ORIGINAL CODE: EPIDOSNREFNO |
|
| APBP | Date of receipt of notice of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA2O |
|
| APAH | Appeal reference modified |
Free format text: ORIGINAL CODE: EPIDOSCREFNO |
|
| APBM | Appeal reference recorded |
Free format text: ORIGINAL CODE: EPIDOSNREFNO |
|
| APBP | Date of receipt of notice of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA2O |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20121012 |
|
| APBQ | Date of receipt of statement of grounds of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA3O |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161207 |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| R26 | Opposition filed (corrected) |
Opponent name: ARCONIC CORPORATION Effective date: 20170907 |
|
| APBU | Appeal procedure closed |
Free format text: ORIGINAL CODE: EPIDOSNNOA9O |
|
| PLAY | Examination report in opposition despatched + time limit |
Free format text: ORIGINAL CODE: EPIDOSNORE2 |
|
| PLBC | Reply to examination report in opposition received |
Free format text: ORIGINAL CODE: EPIDOSNORE3 |
|
| PLAY | Examination report in opposition despatched + time limit |
Free format text: ORIGINAL CODE: EPIDOSNORE2 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230411 |
|
| PUAH | Patent maintained in amended form |
Free format text: ORIGINAL CODE: 0009272 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT MAINTAINED AS AMENDED |
|
| 27A | Patent maintained in amended form |
Effective date: 20240911 |
|
| AK | Designated contracting states |
Kind code of ref document: B2 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R102 Ref document number: 602012026357 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241211 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NO Payment date: 20241029 Year of fee payment: 13 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241211 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: U11 Free format text: ST27 STATUS EVENT CODE: U-0-0-U10-U11 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20251101 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251029 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20251027 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20251027 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20251027 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20251101 Year of fee payment: 14 |