EP2564956A1 - Fabrication method of alloy parts by metal injection molding - Google Patents
Fabrication method of alloy parts by metal injection molding Download PDFInfo
- Publication number
- EP2564956A1 EP2564956A1 EP12185488A EP12185488A EP2564956A1 EP 2564956 A1 EP2564956 A1 EP 2564956A1 EP 12185488 A EP12185488 A EP 12185488A EP 12185488 A EP12185488 A EP 12185488A EP 2564956 A1 EP2564956 A1 EP 2564956A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- binder
- sintering
- alloy
- injection molding
- temperature
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/22—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces for producing castings from a slip
- B22F3/225—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces for producing castings from a slip by injection molding
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/10—Sintering only
- B22F3/1017—Multiple heating or additional steps
- B22F3/1021—Removal of binder or filler
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C33/00—Making ferrous alloys
- C22C33/02—Making ferrous alloys by powder metallurgy
- C22C33/0257—Making ferrous alloys by powder metallurgy characterised by the range of the alloying elements
- C22C33/0278—Making ferrous alloys by powder metallurgy characterised by the range of the alloying elements with at least one alloying element having a minimum content above 5%
- C22C33/0285—Making ferrous alloys by powder metallurgy characterised by the range of the alloying elements with at least one alloying element having a minimum content above 5% with Cr, Co, or Ni having a minimum content higher than 5%
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2998/00—Supplementary information concerning processes or compositions relating to powder metallurgy
- B22F2998/10—Processes characterised by the sequence of their steps
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2999/00—Aspects linked to processes or compositions used in powder metallurgy
Definitions
- the present invention relates to a metal injection molding and a part manufactured by the metal injection molding, and more particularly, to a method of manufacturing a part by using Fe-Cr-based alloy powder in a metal injection molding and the part, that is, the metal injection molding and the part capable of reducing a limitation on a size of the part, increasing a productivity, and providing the part having excellent properties at a low cost as compared with a conventional manufacturing method.
- a metal injection molding that is, a method including a process of mixing power with a binder, a process of injection molding the mixture, a process of removing the binder from the injection moldings, and a process of sintering and forming the debinded injection moldings, thereby manufacturing a product having a net shape that hardly needs finishing processing, is known.
- Parts manufactured by the metal injection molding are mainly used for high value-added precision parts such as a cellular phone hinge requiring abrasion resistance, durability, and mechanical chemical properties including corrosion resistance, high strength, high hardness, and high quality. These parts are manufactured by using iron, nickel, or stainless-based powder.
- the iron, nickel, or stainless-based powder has problems in that the sintering process that is the last forming process is performed at a very high sintering temperature of about 1350°C and costs of electric power consumed for the sintering process and the sintering equipment are very high.
- a conventional powder material is used, adequate properties may not be obtained according to applications.
- a micro-powder injection molding of significantly decreasing a size of the powder is attempted.
- the sintering temperature may decreases by about 100°C as compared with a conventional method.
- a powder price markedly increases as compared with the conventional method, so that there is a problem in that reducing the manufacturing cost cannot be expected.
- Powder injection molding uses various materials such as metal, ceramic, and cemented carbide, and the iron-based material such as stainless that occupies more than 40% of the total materials. Particularly, STS316L has been widely applied. However, as the powder injection molded parts have gradually changed from parts based on a shape to parts as a structural material requiring mechanical properties used for airplanes, cars, medical instruments, STS630(17-4PH) having a high strength has been increasingly used.
- the STS630 is martensite-based precipitation-hardened alloy and is one of high strength alloys having a high corrosion resistance. However, since the stainless has a high sintering temperature, there is a problem in that cost of production significantly increases.
- the present invention provides a method of manufacturing parts which have a low sintering temperature, have an excellent hardness, and can be produced at a low cost to be applied to high value-added precision parts.
- the step of sintering may be performed in a vacuum in a reducing gas or an inert gas atmosphere at a temperature of from 1100°C to less than a melting point of the alloy or at a temperature of 1150°C or more or a temperature of 1200°C or more according to a manufacturing cost and required properties.
- the sintering atmosphere is an atmosphere in which oxide existing at surfaces of the alloy powder is removed during the sintering process.
- the sintering atmosphere is a high-purity hydrogen atmosphere.
- the sintering process is performed at a sintering temperature of from 1100°C to about 1250°C that is a melting point of the alloy powder. Accordingly, the sintering temperature can be decreased by 100 to 250°C as compared with a sintering temperature of 1350°C of stainless-based powder, so that costs of electric power and energy consumed for the sintering process can be significantly reduced.
- an average particle size of the ally powder may range from 0.01 to 100 ⁇ m. Powder having an average particle size of less than 0.01 ⁇ m may cause an significant increase in a manufacturing cost of the powder and in a price of a product. Powder having an average particle size of more than 100 ⁇ m cannot obtain an enough precision and desired properties. Therefore, the powder having the aforementioned particle size may be used.
- the step of removing the binder may be performed by heating the injection moldings at a temperature of from 300 to 700°C in a reducing gas atmosphere and maintaining the temperature for 0.5 to 5 hours.
- a porosity of the part manufactured by the manufacturing method may be a volume fraction of 7% or less, and more preferably, 5% or less. When the porosity exceeds 7%, hardness and properties are decreased, so that the part having the porosity of more than 7% cannot be applied.
- the metal parts manufactured by the metal injection molding according to the present invention have advantages in that a limitation on sizes of the parts is reduced due to characteristics of the manufacturing method, and a continuous production is possible.
- the metal parts have the same or more hardness as compared with metal injection moldings using conventional stainless-based alloy powder but have a lower sintering temperature. Accordingly, high quality and high value-added parts with a competitive price can be manufactured, so that the parts can be used in all fields including cars, computers, electronic components, industrial components, medical instruments, abrasion-resistant components, and so on.
- pores are minimized, and near net shape products with a high density can be manufactured.
- compositions of alloy powder used in the current embodiments are as follows. [Table 1] Chemical compositions of the alloy powder element Cr Si C Cu S B Ni Mo Co Fe C 30-32 1.0-1.8 - 2.2-2.8 - 3.5-4.5 17-19 3.5-4.5 8.8-11 Bal. M 43-46 1.7-2.2 0.17 - 0.2 5.6-6.2 - - - Bal.
- a metal injection molding according to the present invention uses powder having an alloy composition represented as "C” mainly including Fe, Cr, Ni, Co, or the like and an alloy composition represented as "M” mainly including Fe, Cr, B, or the like.
- C alloy composition
- M alloy composition
- the Cr of from 20 to 50wt% or more is mixed with the Fe, so that a sintering temperature can be significantly decreased.
- parts having the same or better mechanical properties as compared with conventional stainless powder injection molded parts can be manufactured.
- FIG. 1 shows a manufacturing process of the metal injection molding according to an embodiment of the present invention.
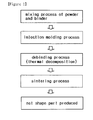
- the metal injection molding includes a mixing process of powder and a binder, an injection molding process of the mixture, a debinding process of removing the binder from the injection moldings by a thermal decomposition, and a process of sintering the debinded moldings, thereby manufacturing near net shape parts.
- a shape of the alloy powder may be close to a spherical shape, and an average particle size of the powder may be 100 ⁇ m or less for a high sintering density and a high numerical precision.
- particles of 40 ⁇ m or less are used.
- the suitable binder is selected so that mixing and injection molding processes are easy and materials having desired properties should be obtained when the used binder is removed after the injection molding process.
- the binder is a material composed of two to five selected from a bonding(bodying) agent, a lubricant, a plasticizer, and a surfactant.
- the total amount of the binder is smaller so as to prevent deformation during the debinding and the sintering processes, and a volume fraction of the binder may range from 30% to 50%.
- the binder used in the embodiment of the present invention is a mixture of ethylene vinyl acetate (EVA) of 20wt% and paraffin wax of 80wt%.
- EVA ethylene vinyl acetate
- the mixing process of the alloy powder and the binder includes weighing the alloy powder and the binder in a predetermined ratio and mixing the alloy powder with the binder in a sigma blade mixer at a temperature ranging from 130 to 160°C for two hours.
- the injection molding process of the mixture includes feeding the alloy mixture into a metal injection molding machine of about 27 ton and injecting the alloy mixture into a metal mold having a predetermined shape at a pressure of 450 bar and a temperature of 120°C.
- the debinding process of removing the binder from the injection moldings includes feeding the moldings into a tube furnace, increasing the temperature up to 300°C in a high-purity hydrogen atmosphere at a speed of 2 °C/min and maintaining the temperature for an hour, increasing the temperature up to 500°C at a speed of 3°C/min and maintaining the temperature for an hour, and increasing the temperature up to 700°C at a speed of 3°C/min and maintaining the temperature for an hour, thereby completely removing the binder.
- a liquid phase transition temperature of each alloy powder having a composition shown in Table. 1 above is measured by a differential thermal analysis (DTA).
- the sintering process is performed in a condition described in Table 2 below at a temperature ranging from 1150°C to less than the liquid phase transition temperature.
- [Table 2] Sintering condition experimental condition specimen sintering temperature and maintaining time 1 C1 1100°C/30mim 2 C2, M2 1150°C/30mim 3 C3, M3 1200°C/30mim 4 M4 1250°C/30mim
- Specimens C1, C2, and C3 shown in Table 2 have the same composition but have different sintering temperatures, and so do specimens M1, M2, and M3.
- the sintering process is performed by increasing the temperatures up to target temperatures of 1100° C, 1150° C, 1200° C, and 1250° C shown in Table 2 at a speed of 5° C/min and maintaining the temperatures in the high-purity hydrogen atmosphere for 30 minutes.
- the sintering process is performed in a reducing gas atmosphere, so that oxide layers formed at surfaces of the alloy powder are removed, and particle bonding proceeds by diffusion.
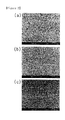
- FIGS. 2 and 3 are pictures taken by a scanning electron microscope (SEM) showing microstructures of metal parts manufactured at the above sintering temperatures. As shown in FIGS. 2 and 3 , as the sintering temperature increases, the volume fraction of pores formed at a grain boundary significantly decreases, and sizes of the pores tend downward. In addition, a result of measuring a porosity and a relative density, that is, a degree of denseness, is shown in following Table 3. [Table 3] A result of measuring a porosity and a relative density of parts specimen porosity (%) relative density (%) C1 4.3 95.68 C2 3.5 96.47 C3 0.01 99.99 M2 0.61 99.39 M3 0.21 99.79 M4 0.05 99.95
- the C1 sintered at the temperature of 1100°C has a relative density of 95.68% that is a relatively high degree. As the sintering temperatures increases, most specimens have high relative densities of more than 99%.
- the C1 according to the embodiment of the present invention is sintered at a very low sintering temperature but has a similar hardness as compared with STS316L, the C2 has a better hardness, and the C3 and the M2 have about three times the hardness of the STS316L and have the same or more hardness as compared with STS630.
- the parts having high physical properties at a low cost as compared with the stainless powder injection moldings can be manufactured, so that the parts can replace the STS316L and the STS630.
- the M3 and the M4 according to the present invention have lower sintering temperatures as those of the stainless powder injection moldings but have the excellent hardnesses of 747 and 1059, respectively, as compared with the stainless powder injection moldings.
- Present invention is applicable to the field of powder injection molding.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Chemical & Material Sciences (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Powder Metallurgy (AREA)
Abstract
A method of manufacturing an alloy part comprises mixing an alloy powder and a binder, the alloy powder having a composition including 40 to 50wt% Cr, 1 to 2.5wt% Si, 0.5wt% or less C, 5.6 to 6.2wt% B and the remainder Fe and unavoidable impurities; performing an injection molding on the mixture to form the injection moldings to have a shape of the part;removing the binder from the injection moldings; and sintering the injection moldings from which the binder is removed.
Description
- The present invention relates to a metal injection molding and a part manufactured by the metal injection molding, and more particularly, to a method of manufacturing a part by using Fe-Cr-based alloy powder in a metal injection molding and the part, that is, the metal injection molding and the part capable of reducing a limitation on a size of the part, increasing a productivity, and providing the part having excellent properties at a low cost as compared with a conventional manufacturing method.
- As a method of manufacturing precision parts having complex shapes used for cars, computers, electronic components, industrial components, medical instruments, and abrasion-resistant components, there are cutting, die casting, precision casting, and powder metallurgy, and so on. However, these methods have problems in that a manufacturing cost is high, productivity decreases, desired properties cannot be obtained due to a limitation on usable constituent materials of an alloy, and complex 3D shapes cannot be obtained, and so on.
- In order to solve the problems of formability, processability, and productivity, a metal injection molding, that is, a method including a process of mixing power with a binder, a process of injection molding the mixture, a process of removing the binder from the injection moldings, and a process of sintering and forming the debinded injection moldings, thereby manufacturing a product having a net shape that hardly needs finishing processing, is known.
- Parts manufactured by the metal injection molding are mainly used for high value-added precision parts such as a cellular phone hinge requiring abrasion resistance, durability, and mechanical chemical properties including corrosion resistance, high strength, high hardness, and high quality. These parts are manufactured by using iron, nickel, or stainless-based powder.
- However, the iron, nickel, or stainless-based powder has problems in that the sintering process that is the last forming process is performed at a very high sintering temperature of about 1350°C and costs of electric power consumed for the sintering process and the sintering equipment are very high. In addition, when a conventional powder material is used, adequate properties may not be obtained according to applications.
- Accordingly, in order to decrease the sintering temperature and increase a forming precision, a micro-powder injection molding (PIM) of significantly decreasing a size of the powder is attempted. In this method, by decreasing the size of the powder, the sintering temperature may decreases by about 100°C as compared with a conventional method. However, a powder price markedly increases as compared with the conventional method, so that there is a problem in that reducing the manufacturing cost cannot be expected.
- Powder injection molding uses various materials such as metal, ceramic, and cemented carbide, and the iron-based material such as stainless that occupies more than 40% of the total materials. Particularly, STS316L has been widely applied. However, as the powder injection molded parts have gradually changed from parts based on a shape to parts as a structural material requiring mechanical properties used for airplanes, cars, medical instruments, STS630(17-4PH) having a high strength has been increasingly used. The STS630 is martensite-based precipitation-hardened alloy and is one of high strength alloys having a high corrosion resistance. However, since the stainless has a high sintering temperature, there is a problem in that cost of production significantly increases.
- In order to solve the aforementioned problems, the present invention provides a method of manufacturing parts which have a low sintering temperature, have an excellent hardness, and can be produced at a low cost to be applied to high value-added precision parts.
- According to an aspect of the present invention, there is provided a method of manufacturing an alloy part according to claim 1.
- In addition, the step of sintering may be performed in a vacuum in a reducing gas or an inert gas atmosphere at a temperature of from 1100°C to less than a melting point of the alloy or at a temperature of 1150°C or more or a temperature of 1200°C or more according to a manufacturing cost and required properties. The sintering atmosphere is an atmosphere in which oxide existing at surfaces of the alloy powder is removed during the sintering process. Preferably, the sintering atmosphere is a high-purity hydrogen atmosphere.
- In addition, the sintering process is performed at a sintering temperature of from 1100°C to about 1250°C that is a melting point of the alloy powder. Accordingly, the sintering temperature can be decreased by 100 to 250°C as compared with a sintering temperature of 1350°C of stainless-based powder, so that costs of electric power and energy consumed for the sintering process can be significantly reduced.
- In addition, an average particle size of the ally powder may range from 0.01 to 100µm. Powder having an average particle size of less than 0.01µm may cause an significant increase in a manufacturing cost of the powder and in a price of a product. Powder having an average particle size of more than 100µm cannot obtain an enough precision and desired properties. Therefore, the powder having the aforementioned particle size may be used.
- In addition, the step of removing the binder may be performed by heating the injection moldings at a temperature of from 300 to 700°C in a reducing gas atmosphere and maintaining the temperature for 0.5 to 5 hours.
- In addition, a porosity of the part manufactured by the manufacturing method may be a volume fraction of 7% or less, and more preferably, 5% or less. When the porosity exceeds 7%, hardness and properties are decreased, so that the part having the porosity of more than 7% cannot be applied.
- As described above, the metal parts manufactured by the metal injection molding according to the present invention have advantages in that a limitation on sizes of the parts is reduced due to characteristics of the manufacturing method, and a continuous production is possible. In addition, the metal parts have the same or more hardness as compared with metal injection moldings using conventional stainless-based alloy powder but have a lower sintering temperature. Accordingly, high quality and high value-added parts with a competitive price can be manufactured, so that the parts can be used in all fields including cars, computers, electronic components, industrial components, medical instruments, abrasion-resistant components, and so on.
- In addition, according to the metal injection molding according to the present invention, pores are minimized, and near net shape products with a high density can be manufactured.
-
-
FIG. 1 is a flowchart schematically showing a manufacturing process according to the present invention. -
FIG. 2 is a picture taken by a scanning electron microscope (SEM) showing a degree of denseness of a metal part manufactured according to an embodiment of the present invention. -
FIG. 3 is a picture taken by a SEM showing a degree of denseness of a metal part manufactured according to another embodiment of the present invention. - The present invention will now be described more fully with reference to the accompanying drawings, in which exemplary embodiments of the invention are shown. The exemplary embodiments should be considered in descriptive sense only and not for purposes of limitation.
- Chemical compositions of alloy powder used in the current embodiments are as follows.
[Table 1] Chemical compositions of the alloy powder element Cr Si C Cu S B Ni Mo Co Fe C 30-32 1.0-1.8 - 2.2-2.8 - 3.5-4.5 17-19 3.5-4.5 8.8-11 Bal. M 43-46 1.7-2.2 0.17 - 0.2 5.6-6.2 - - - Bal. - As shown in Table 1 above, a metal injection molding according to the present invention uses powder having an alloy composition represented as "C" mainly including Fe, Cr, Ni, Co, or the like and an alloy composition represented as "M" mainly including Fe, Cr, B, or the like. As described above, the Cr of from 20 to 50wt% or more is mixed with the Fe, so that a sintering temperature can be significantly decreased. In addition, as shown in an experimental result below, parts having the same or better mechanical properties as compared with conventional stainless powder injection molded parts can be manufactured.
-
FIG. 1 shows a manufacturing process of the metal injection molding according to an embodiment of the present invention. Referring toFIG. 1 , the metal injection molding includes a mixing process of powder and a binder, an injection molding process of the mixture, a debinding process of removing the binder from the injection moldings by a thermal decomposition, and a process of sintering the debinded moldings, thereby manufacturing near net shape parts. - In the mixing process, a shape of the alloy powder may be close to a spherical shape, and an average particle size of the powder may be 100µm or less for a high sintering density and a high numerical precision. In the current embodiment of the present invention, particles of 40µm or less are used.
- In addition, the most important work in the mixing process is to select a suitable binder. The suitable binder is selected so that mixing and injection molding processes are easy and materials having desired properties should be obtained when the used binder is removed after the injection molding process. The binder is a material composed of two to five selected from a bonding(bodying) agent, a lubricant, a plasticizer, and a surfactant. As long as formability is guaranteed during the injection molding, it is preferable that the total amount of the binder is smaller so as to prevent deformation during the debinding and the sintering processes, and a volume fraction of the binder may range from 30% to 50%.
- The binder used in the embodiment of the present invention is a mixture of ethylene vinyl acetate (EVA) of 20wt% and paraffin wax of 80wt%. The mixing process of the alloy powder and the binder includes weighing the alloy powder and the binder in a predetermined ratio and mixing the alloy powder with the binder in a sigma blade mixer at a temperature ranging from 130 to 160°C for two hours.
- The injection molding process of the mixture includes feeding the alloy mixture into a metal injection molding machine of about 27 ton and injecting the alloy mixture into a metal mold having a predetermined shape at a pressure of 450 bar and a temperature of 120°C.
- The debinding process of removing the binder from the injection moldings includes feeding the moldings into a tube furnace, increasing the temperature up to 300°C in a high-purity hydrogen atmosphere at a speed of 2 °C/min and maintaining the temperature for an hour, increasing the temperature up to 500°C at a speed of 3°C/min and maintaining the temperature for an hour, and increasing the temperature up to 700°C at a speed of 3°C/min and maintaining the temperature for an hour, thereby completely removing the binder.
- A liquid phase transition temperature of each alloy powder having a composition shown in Table. 1 above is measured by a differential thermal analysis (DTA). The sintering process is performed in a condition described in Table 2 below at a temperature ranging from 1150°C to less than the liquid phase transition temperature.
[Table 2] Sintering condition experimental condition specimen sintering temperature and maintaining time 1 C1 1100°C/30mim 2 C2, M2 1150°C/30mim 3 C3, M3 1200°C/30mim 4 M4 1250°C/30mim - Specimens C1, C2, and C3 shown in Table 2 have the same composition but have different sintering temperatures, and so do specimens M1, M2, and M3. The sintering process is performed by increasing the temperatures up to target temperatures of 1100° C, 1150° C, 1200° C, and 1250° C shown in Table 2 at a speed of 5° C/min and maintaining the temperatures in the high-purity hydrogen atmosphere for 30 minutes. As described above, the sintering process is performed in a reducing gas atmosphere, so that oxide layers formed at surfaces of the alloy powder are removed, and particle bonding proceeds by diffusion.
-
FIGS. 2 and3 are pictures taken by a scanning electron microscope (SEM) showing microstructures of metal parts manufactured at the above sintering temperatures. As shown inFIGS. 2 and3 , as the sintering temperature increases, the volume fraction of pores formed at a grain boundary significantly decreases, and sizes of the pores tend downward. In addition, a result of measuring a porosity and a relative density, that is, a degree of denseness, is shown in following Table 3.[Table 3] A result of measuring a porosity and a relative density of parts specimen porosity (%) relative density (%) C1 4.3 95.68 C2 3.5 96.47 C3 0.01 99.99 M2 0.61 99.39 M3 0.21 99.79 M4 0.05 99.95 - As shown in Table 3, the C1 sintered at the temperature of 1100°C has a relative density of 95.68% that is a relatively high degree. As the sintering temperatures increases, most specimens have high relative densities of more than 99%.
- By measuring a hardness of the parts according to the current embodiment, a result shown in Table 4 is obtained.
[Table 4] A result of measuring a hardness of parts specimen hardness (VHN) note C1 94 embodiment C2 115 embodiment C3 319 embodiment M2 353 embodiment M3 747 embodiment M4 1059 embodiment STS316L 97 comparative example STS630 275 comparative example STS440C 543 comparative example - As shown in Table 4, the C1 according to the embodiment of the present invention is sintered at a very low sintering temperature but has a similar hardness as compared with STS316L, the C2 has a better hardness, and the C3 and the M2 have about three times the hardness of the STS316L and have the same or more hardness as compared with STS630. Namely, the parts having high physical properties at a low cost as compared with the stainless powder injection moldings can be manufactured, so that the parts can replace the STS316L and the STS630.
- In addition, it can be seen that the M3 and the M4 according to the present invention have lower sintering temperatures as those of the stainless powder injection moldings but have the excellent hardnesses of 747 and 1059, respectively, as compared with the stainless powder injection moldings.
- Present invention is applicable to the field of powder injection molding.
Claims (7)
- A method of manufacturing an alloy part, comprising:mixing an alloy powder and a binder, the alloy powder having a composition including40 to 50wt% Cr,1 to 2.5wt% Si,0.5wt% or less C,5.6 to 6.2wt% B andthe remainder Fe and unavoidable impurities;performing an injection molding on the mixture to form the injection moldings to have a shape of the part;removing the binder from the injection moldings; andsintering the injection moldings from which the binder is removed.
- The method of claim 1, wherein the step of sintering is performed in a vacuum in a reducing gas or an inert gas atmosphere at a temperature of from 1100°C to less than a melting point of the alloy.
- The method of claim 2, wherein the sintering temperature ranges from 1150°C to less than the melting point of the alloy.
- The method of claim 1, wherein an average size of the alloy powder ranges from 0.01 to 100µm.
- The method of claim 1, wherein the step of removing the binder is performed by heating the injection moldings at a temperature of from 300 to 700°C in a reducing gas, an inert gas, or a mixture of the reducing gas and the inert gas atmosphere and maintaining the temperature for 0.5 to 5 hours.
- An alloy part manufactured through a method comprising:mixing an alloy powder and a binder, the alloy powder having a composition including40 to 50wt% Cr,1 to 2.5wt% Si,0.5wt% or less C,5.6 to 6.2wt% B andthe remainder Fe and unavoidable impurities;performing an injection molding on the mixture to form the injection moldings to have a shape of the part;removing the binder from the injection moldings; andsintering the injection moldings from which the binder is removed.
- The alloy part of any one of claims 6, wherein a porosity of the part is a volume fraction of 7% or less.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020060058373A KR100768700B1 (en) | 2006-06-28 | 2006-06-28 | Manufacturing method and alloy parts of alloy parts using metal injection molding |
| EP07708670A EP2043801A4 (en) | 2006-06-28 | 2007-01-30 | METHOD FOR MANUFACTURING ALLOY PARTS MOLDED BY INJECTION OF METAL, AND ALLOY PARTS THUS OBTAINED |
Related Parent Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP07708670.0 Division | 2007-01-30 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP2564956A1 true EP2564956A1 (en) | 2013-03-06 |
Family
ID=38815316
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12185488A Withdrawn EP2564956A1 (en) | 2006-06-28 | 2007-01-30 | Fabrication method of alloy parts by metal injection molding |
| EP07708670A Withdrawn EP2043801A4 (en) | 2006-06-28 | 2007-01-30 | METHOD FOR MANUFACTURING ALLOY PARTS MOLDED BY INJECTION OF METAL, AND ALLOY PARTS THUS OBTAINED |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP07708670A Withdrawn EP2043801A4 (en) | 2006-06-28 | 2007-01-30 | METHOD FOR MANUFACTURING ALLOY PARTS MOLDED BY INJECTION OF METAL, AND ALLOY PARTS THUS OBTAINED |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20090297396A1 (en) |
| EP (2) | EP2564956A1 (en) |
| JP (1) | JP2009542905A (en) |
| KR (1) | KR100768700B1 (en) |
| CN (1) | CN101479063B (en) |
| WO (1) | WO2008002001A1 (en) |
Families Citing this family (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101579160B (en) * | 2009-06-05 | 2014-08-06 | 刘世华 | Stainless steel zipper manufactured by metal injection molding and preparation method thereof |
| MX360038B (en) * | 2010-12-30 | 2018-10-18 | Hoeganaes Ab Publ | IRON BASED POWDER FOR MOLDING BY DUST INJECTION. |
| KR101350944B1 (en) * | 2011-10-21 | 2014-01-16 | 포항공과대학교 산학협력단 | Ferrous-alloys for powder injection molding |
| AU2013320366B2 (en) * | 2012-09-21 | 2017-12-07 | Hoganas Ab (Publ) | New powder, powder composition, method for use thereof and use of the powder and powder composition |
| KR20140048428A (en) * | 2012-10-15 | 2014-04-24 | 현대자동차주식회사 | Method for manufacturing of control finger using with metal powder injection molding |
| WO2015102732A2 (en) * | 2013-10-25 | 2015-07-09 | Golden Intellectual Property, Llc | Amorphous alloy containing feedstock for powder injection molding |
| CN103990803B (en) * | 2014-05-28 | 2017-01-11 | 厦门市超日精密模具有限公司 | Tungsten-molybdenum alloy powder injection mould and technology thereof |
| KR20160023365A (en) | 2014-08-22 | 2016-03-03 | 박상준 | Method for Producing Articles Using Injection Molding of Alloy |
| CN106119662B (en) * | 2016-07-28 | 2018-01-02 | 洛阳轴研科技股份有限公司 | A kind of cobalt-chromium-tungsten alloy material, cobalt-chromium-tungsten alloy ball for ball-screw bearing and preparation method thereof, ball-screw bearing |
| CN106498261A (en) * | 2016-11-21 | 2017-03-15 | 常熟市张桥华丰铸造五金厂 | A kind of multiduty high-performance foundry goods |
| CN108746630A (en) * | 2018-06-25 | 2018-11-06 | 长春中科昊融新材料研究有限公司 | Reduce the method that sintering temperature prepares metal injection moulding feeding |
| CN114086078B (en) * | 2020-08-25 | 2025-05-06 | 华为技术有限公司 | Fe-Mn-Al-C series lightweight steel and preparation method thereof, terminal, steel structure and electronic equipment |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4721599A (en) * | 1985-04-26 | 1988-01-26 | Hitachi Metals, Ltd. | Method for producing metal or alloy articles |
| EP1033194A1 (en) * | 1998-09-18 | 2000-09-06 | Injex Corporation | Metal sintere body and production method thereof |
| US6299664B1 (en) * | 1998-02-04 | 2001-10-09 | Mitsubishi Denki Kabushiki Kaisha | Method of manufacturing sliding part and vortex flow generator for injection valve manufactured by that method |
| US6309592B1 (en) * | 2000-04-05 | 2001-10-30 | Lite-On It Corporation | Method for manufacturing roller carrier of vibration balance device |
Family Cites Families (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4052802A (en) * | 1976-02-23 | 1977-10-11 | Caterpillar Tractor Co. | Ground-engaging tool with wear-resistant insert |
| US4194900A (en) * | 1978-10-05 | 1980-03-25 | Toyo Kohan Co., Ltd. | Hard alloyed powder and method of making the same |
| JPS5976860A (en) | 1982-10-25 | 1984-05-02 | Hitachi Metals Ltd | Permanent magnet material |
| JPS60155650A (en) | 1984-04-03 | 1985-08-15 | Nippon Piston Ring Co Ltd | Sliding member for power machine |
| US5338508A (en) * | 1988-07-13 | 1994-08-16 | Kawasaki Steel Corporation | Alloy steel powders for injection molding use, their compounds and a method for making sintered parts from the same |
| US5030519A (en) * | 1990-04-24 | 1991-07-09 | Amorphous Metals Technologies, Inc. | Tungsten carbide-containing hard alloy that may be processed by melting |
| JP3049294B2 (en) * | 1993-06-11 | 2000-06-05 | 大同特殊鋼株式会社 | Decorative parts |
| US6171657B1 (en) * | 1995-12-18 | 2001-01-09 | Bender Machine, Inc. | Method of coating yankee dryers against wear |
| JPH1161360A (en) * | 1997-08-13 | 1999-03-05 | Hatsuto:Kk | Stainless steel sintered body and method of manufacturing the same |
| JPH11100633A (en) * | 1997-09-29 | 1999-04-13 | Toshiba Mach Co Ltd | Thermal insulation member and method of manufacturing the same |
| FR2785559B1 (en) * | 1998-11-10 | 2001-03-02 | Metals Process Systems | METHOD FOR THE MANUFACTURE BY METALLURGY OF POWDERS OF AUTOBRASANT SHAPED PARTS |
| JP3856294B2 (en) * | 2001-11-30 | 2006-12-13 | セイコーエプソン株式会社 | Stainless steel powder for sintering, granulated powder for manufacturing sintered stainless steel, and sintered stainless steel |
| JP4849770B2 (en) * | 2003-02-13 | 2012-01-11 | 三菱製鋼株式会社 | Alloy steel powder for metal injection molding with improved sinterability |
| CN1180908C (en) * | 2003-09-30 | 2004-12-22 | 北京科技大学 | A kind of method for preparing Kovar alloy electronic packaging box body |
| US20050163645A1 (en) * | 2004-01-28 | 2005-07-28 | Borgwarner Inc. | Method to make sinter-hardened powder metal parts with complex shapes |
| KR100650409B1 (en) * | 2004-12-17 | 2006-11-27 | (주)엠티아이지 | Manufacturing method of complex shape material using powder injection molding and material produced accordingly |
-
2006
- 2006-06-28 KR KR1020060058373A patent/KR100768700B1/en not_active Expired - Fee Related
-
2007
- 2007-01-30 EP EP12185488A patent/EP2564956A1/en not_active Withdrawn
- 2007-01-30 JP JP2009517946A patent/JP2009542905A/en active Pending
- 2007-01-30 WO PCT/KR2007/000514 patent/WO2008002001A1/en not_active Ceased
- 2007-01-30 CN CN200780024689XA patent/CN101479063B/en not_active Expired - Fee Related
- 2007-01-30 US US12/306,778 patent/US20090297396A1/en not_active Abandoned
- 2007-01-30 EP EP07708670A patent/EP2043801A4/en not_active Withdrawn
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4721599A (en) * | 1985-04-26 | 1988-01-26 | Hitachi Metals, Ltd. | Method for producing metal or alloy articles |
| US6299664B1 (en) * | 1998-02-04 | 2001-10-09 | Mitsubishi Denki Kabushiki Kaisha | Method of manufacturing sliding part and vortex flow generator for injection valve manufactured by that method |
| EP1033194A1 (en) * | 1998-09-18 | 2000-09-06 | Injex Corporation | Metal sintere body and production method thereof |
| US6309592B1 (en) * | 2000-04-05 | 2001-10-30 | Lite-On It Corporation | Method for manufacturing roller carrier of vibration balance device |
Also Published As
| Publication number | Publication date |
|---|---|
| KR100768700B1 (en) | 2007-10-19 |
| US20090297396A1 (en) | 2009-12-03 |
| WO2008002001A1 (en) | 2008-01-03 |
| EP2043801A4 (en) | 2011-04-13 |
| EP2043801A1 (en) | 2009-04-08 |
| JP2009542905A (en) | 2009-12-03 |
| CN101479063A (en) | 2009-07-08 |
| CN101479063B (en) | 2011-12-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US20090297396A1 (en) | Fabrication method of alloy parts by metal injection molding and the alloy parts | |
| KR102592186B1 (en) | Cemented carbide powder for additive manufacturing | |
| CN104874797B (en) | A kind of forming method of hard alloy FGM | |
| CN1312078C (en) | Submicron grain Ti(C,N)-base cermet and its prepn process | |
| US20140077426A1 (en) | Method of manufacturing powder injection-molded body | |
| US20200346365A1 (en) | Cemented carbide powders for additive manufacturing | |
| CN104946914B (en) | A kind of forming method of Metal Substrate functional gradient composite materials | |
| JPWO2010008004A1 (en) | Hard powder, method for producing hard powder, and sintered hard alloy | |
| CN102839311B (en) | Metal ceramic and preparation method thereof | |
| JP2009544841A (en) | Iron-based powder | |
| CN115365489A (en) | Composition for injection molding, injection molded body, and method for producing titanium sintered body | |
| JP2012077352A (en) | Cemented carbide alloy, and cemented carbide tool | |
| JP6667264B2 (en) | Manufacturing method of high-rigidity iron-based sintered alloy | |
| JP2014169471A (en) | Ni-BASED INTERMETALLIC COMPOUND SINTERED BODY, AND PRODUCING METHOD THEREFOR | |
| KR100570551B1 (en) | Manufacturing method of aluminum alloy powder with excellent moldability | |
| JPH0499146A (en) | Powder sintered material and its manufacture | |
| CN115386775B (en) | High-elasticity-modulus metal ceramic material and preparation method thereof | |
| JPH06240381A (en) | Production of ti alloy sintered compact by injection-molding of metal powder | |
| JPH10317009A (en) | Manufacturing method of stainless sintered body | |
| Handtrack et al. | Additive Manufacturing of Tungsten Heavy Alloys–A Technology Assessment of sinter-based AM Processes | |
| JPH11181541A (en) | Manufacturing method of stainless sintered body | |
| JP2758569B2 (en) | Method for producing iron-based sintered body by metal powder injection molding method | |
| Matula | Influence of binder composition on structure and properties of carbide alloyed composite manufactured with the PIM method | |
| JPH04280903A (en) | Manufacture of cemented carbide powder for injection molding and cemented carbide sintered product | |
| JPH11315305A (en) | Manufacturing method of sintered body |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AC | Divisional application: reference to earlier application |
Ref document number: 2043801 Country of ref document: EP Kind code of ref document: P |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20130907 |