EP1411298A2 - System for optimizing combustion processes by means of direct measures inside the hearth - Google Patents
System for optimizing combustion processes by means of direct measures inside the hearth Download PDFInfo
- Publication number
- EP1411298A2 EP1411298A2 EP20010903810 EP01903810A EP1411298A2 EP 1411298 A2 EP1411298 A2 EP 1411298A2 EP 20010903810 EP20010903810 EP 20010903810 EP 01903810 A EP01903810 A EP 01903810A EP 1411298 A2 EP1411298 A2 EP 1411298A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- probes
- boiler
- sampling probe
- sampling
- furnace
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000002485 combustion reaction Methods 0.000 title claims abstract description 20
- 239000000523 sample Substances 0.000 claims abstract description 60
- 238000005259 measurement Methods 0.000 claims abstract description 27
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims abstract description 12
- 239000012528 membrane Substances 0.000 claims abstract description 10
- 238000000605 extraction Methods 0.000 claims abstract description 7
- 238000012986 modification Methods 0.000 claims abstract description 5
- 230000004048 modification Effects 0.000 claims abstract description 5
- 238000005070 sampling Methods 0.000 claims description 34
- 239000007789 gas Substances 0.000 claims description 19
- 238000000034 method Methods 0.000 claims description 9
- 238000004458 analytical method Methods 0.000 claims description 8
- 230000003750 conditioning effect Effects 0.000 claims description 8
- 238000006073 displacement reaction Methods 0.000 claims description 8
- 239000012530 fluid Substances 0.000 claims description 6
- 238000003780 insertion Methods 0.000 claims description 6
- 230000037431 insertion Effects 0.000 claims description 6
- 238000013461 design Methods 0.000 claims description 5
- 238000013459 approach Methods 0.000 claims description 3
- 239000002826 coolant Substances 0.000 claims description 3
- 239000003344 environmental pollutant Substances 0.000 claims description 3
- 238000012544 monitoring process Methods 0.000 claims description 3
- 231100000719 pollutant Toxicity 0.000 claims description 3
- 229910010293 ceramic material Inorganic materials 0.000 claims description 2
- 238000004140 cleaning Methods 0.000 claims description 2
- 239000000654 additive Substances 0.000 claims 2
- 239000000428 dust Substances 0.000 claims 2
- 239000002699 waste material Substances 0.000 claims 2
- 235000002918 Fraxinus excelsior Nutrition 0.000 claims 1
- 239000002956 ash Substances 0.000 claims 1
- 238000007664 blowing Methods 0.000 claims 1
- 238000001816 cooling Methods 0.000 claims 1
- 239000007788 liquid Substances 0.000 claims 1
- 239000007800 oxidant agent Substances 0.000 claims 1
- 239000007787 solid Substances 0.000 claims 1
- 239000008247 solid mixture Substances 0.000 claims 1
- 239000004449 solid propellant Substances 0.000 claims 1
- 231100000331 toxic Toxicity 0.000 claims 1
- 230000002588 toxic effect Effects 0.000 claims 1
- 238000012512 characterization method Methods 0.000 abstract description 7
- 239000000446 fuel Substances 0.000 description 4
- 238000007689 inspection Methods 0.000 description 3
- 238000004519 manufacturing process Methods 0.000 description 3
- 239000003245 coal Substances 0.000 description 2
- 238000011161 development Methods 0.000 description 2
- -1 gasoil Substances 0.000 description 2
- 238000005057 refrigeration Methods 0.000 description 2
- UGFAIRIUMAVXCW-UHFFFAOYSA-N Carbon monoxide Chemical compound [O+]#[C-] UGFAIRIUMAVXCW-UHFFFAOYSA-N 0.000 description 1
- 238000009825 accumulation Methods 0.000 description 1
- QVGXLLKOCUKJST-UHFFFAOYSA-N atomic oxygen Chemical compound [O] QVGXLLKOCUKJST-UHFFFAOYSA-N 0.000 description 1
- 230000002238 attenuated effect Effects 0.000 description 1
- 230000005540 biological transmission Effects 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000006227 byproduct Substances 0.000 description 1
- 229910002091 carbon monoxide Inorganic materials 0.000 description 1
- 239000003795 chemical substances by application Substances 0.000 description 1
- 239000000567 combustion gas Substances 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 239000012809 cooling fluid Substances 0.000 description 1
- 238000009826 distribution Methods 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000011156 evaluation Methods 0.000 description 1
- 239000000295 fuel oil Substances 0.000 description 1
- 230000004927 fusion Effects 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 238000002156 mixing Methods 0.000 description 1
- 229910052760 oxygen Inorganic materials 0.000 description 1
- 239000001301 oxygen Substances 0.000 description 1
- 229920001610 polycaprolactone Polymers 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 239000000047 product Substances 0.000 description 1
- 239000000725 suspension Substances 0.000 description 1
- 238000012546 transfer Methods 0.000 description 1
Images


Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F23—COMBUSTION APPARATUS; COMBUSTION PROCESSES
- F23N—REGULATING OR CONTROLLING COMBUSTION
- F23N5/00—Systems for controlling combustion
- F23N5/02—Systems for controlling combustion using devices responsive to thermal changes or to thermal expansion of a medium
- F23N5/08—Systems for controlling combustion using devices responsive to thermal changes or to thermal expansion of a medium using light-sensitive elements
- F23N5/082—Systems for controlling combustion using devices responsive to thermal changes or to thermal expansion of a medium using light-sensitive elements using electronic means
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F23—COMBUSTION APPARATUS; COMBUSTION PROCESSES
- F23N—REGULATING OR CONTROLLING COMBUSTION
- F23N5/00—Systems for controlling combustion
- F23N5/003—Systems for controlling combustion using detectors sensitive to combustion gas properties
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F23—COMBUSTION APPARATUS; COMBUSTION PROCESSES
- F23N—REGULATING OR CONTROLLING COMBUSTION
- F23N5/00—Systems for controlling combustion
- F23N5/02—Systems for controlling combustion using devices responsive to thermal changes or to thermal expansion of a medium
- F23N5/022—Systems for controlling combustion using devices responsive to thermal changes or to thermal expansion of a medium using electronic means
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F23—COMBUSTION APPARATUS; COMBUSTION PROCESSES
- F23N—REGULATING OR CONTROLLING COMBUSTION
- F23N2225/00—Measuring
- F23N2225/08—Measuring temperature
- F23N2225/16—Measuring temperature burner temperature
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F23—COMBUSTION APPARATUS; COMBUSTION PROCESSES
- F23N—REGULATING OR CONTROLLING COMBUSTION
- F23N2229/00—Flame sensors
- F23N2229/18—Flame sensor cooling means
Definitions
- the system object of the patent consists, in its basic version, of a probe or probes and in a variety of openings, that by its special characteristics, allow the accomplishment of measurements or characterisations in high temperature areas (nearness of the burners, or any other area of the interior of the furnace of industrial boilers). These local measurements intend to optimise the operation of each burner, allowing the global improvement of parameters like combustion efficiency, loss on ignition, polluting agents formation and slagging processes.
- the small holes are drilled through the membranes which join the water tubes making up the water walls of these type of facilities, making feasible the mentioned local measurements with no need to undertake substantial modifications in the boiler.
- the probe is designed taking into account the limitation entailed by the membranes width (typically around 20 mm) and, therefore, the openings carried out on them.
- Industrial furnaces are facilities where the fuel (pulverised coal, fueloil, gasoil, gas, etc) is injected into the combustion chamber through burners tips, where it reaches the ignition point and bums to produce heat. This heat is transmitted to the water that circulates through the pipes that make up the boiler walls, and to other heat exchanging equipment, producing steam at high pressure and temperature.
- the energy of this steam may have a use in several industrial operations or it may be recovered as mechanical energy in a turbine, with the possibility to be subsequently transformed into electric energy by means of an alternator connected to the turbine.
- This invention involves a system which allows measurements to be taken in any area of the interior of the furnace of industrial boilers, specially near the burners. Some examples of this type of measurement are the evaluation of local levels of gas concentrations, temperatures, heat flows, and even image capture, in these areas of high temperature and very limited access in boilers of traditional design. The aim of these measurements is to identify the combustion conditions at any particular point inside the boilers, in order to be able to optimise heat rate, consumption of auxiliaries, and generation of pollutants and slagging.
- the system allows these measurements to be made through small openings made in the membranes which join the tubes making up the water walls of the boiler.
- the width of these openings (around 14 mm) is limited by the width of the membranes themselves (around 20 mm), while the height is unlimited, due to the geometry of the membranes.
- This new concept for measurement inside the furnace of industrial boilers makes it possible to place the openings in any location required, without being limited to those inspection ports included in the original design of the boiler, and permits the direct measurement of combustion conditions inside the furnace. In this way, it is possible to take measurements at the level of each burner in the boiler, without any significant structural modifications to the unit.
- a water-cooled probe either made of or covered by ceramic material, has been specially designed for insertion through these openings, which additionally is able to withstand the high temperatures (1400 - 1700 °C) in these areas of the furnace.
- An optional upgrade to the system allows automatic operation by means of the following: motorization of the probe (insertion - extraction, lateral movement); a system of continuous treatment and analysis of the gas samples collected or of the data provided by the sensors inserted into the furnace by the probe; a cleaning system using a compressed air counterflow which guarantees the autonomy of the system between measurements; advanced monitoring software which, in addition to controlling the operation of the entire automated system and the correct processing of the results obtained, provides operational recommendations to the operator of the plant. These recommendations are based on results and the experience in the optimisation of this process.
- the invention described is applicable, to the optimisation of any type of burner, for example those in industrial furnaces.
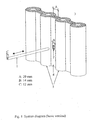
- Figure 1 presents a schematic drawing of the system in its basic version, where the sampling probe (1) is introduced through the opening (2) inside the furnace boiler (3).
- This small opening (2) is made in the membrane (4) which join the tubes (5) making up the water walls of the boiler, close to a facility burner.
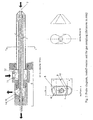
- Figure 2 represents a probe longitudinal section (1) in its cooled and gas sampling variant; the outer socket (6) of entrance and exit of the coolant fluid and its circulation once inside the probe is shown. Also, the sample aspiration conduct can be observed (7).
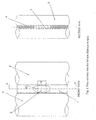
- Figure 3 presents a front view and a cross section of the opening (2) made in the membrane (4) between the tubes (5), for the sampling probe variant (1) shown in Figure 2 (cooled and for gas sampling).
- FIG 4 presents a schematic drawing of an automated system version, specifically its variant for gas sampling, in which the sampling probes displacement can only be of insertion-extraction (a sampling probe by orifice), or with additional lateral displacement (a sampling probe for several orifices).
- Figure 5 shows the schematic drawing of the required elements for this variant.
- the access openings (2) are distributed throughout the boiler close to each burner.
- the water cooled probe is specially designed to support the high existing temperatures in this zone (between 1400 and 1700°C) and to accede to the interior of the boiler through the described orifices.
- a tube of rectangular section can be used for its construction (14 x 12 mm sides and 1 mm thick) and two half tubes (7 mm radius and 1 mm thickness) welded as shown in the figure Section A-a.
- the three resulting cameras can be appreciated (8, 9, 10) through which the refrigeration fluid, for example, water, flows.
- the chamber in the middle (9) is crossed by a 6 mm diameter tube through which the gas sample is extracted to be analysed.
- These elements are assembled at the probes end by means of two half cones and two triangular plates, according to what is observed in the detail of the probes end ( Figure 2).
- an outer socket is arranged (6) allowing the exit and entrance of the refrigeration fluid and of the sample collection tube.
- the route described by the cooling fluid is as follows: it enters through the orifice (11) into the A chamber socket (12), flowing then into the two sampling probe outer chamber (8) and (10). After reaching the end of the sampling probe the fluid returns through the central chamber (9) until reaching the B socket chamber (13) where it leaves the sampling probe through the orifice (14).
- FIG. 4 A system automation schematic drawing is presented in Figure 4.In this figure, the sampling probe (11), being cooled or not, is coupled to a pneumatic cylinder (15), controlled by a multiway valve (16), to insert or retract the probe in or out of the furnace boiler(3).
- the sample collected by the probe passes through a heated filter to eliminate ash in suspension, and then goes to a set of valves which either send the sample to the conditioning system, or send pressurised air towards the heated filter and the probe, giving rise to a countercurrent which cleans both of these items.
- a typical sample conditioning system (19) is made up of a condenser, a cooler, a filter and a pump. This conditioning system may be housed in a cabinet (20) located on the cylinder-probe assembly support, which can also be used to house the valves, or in an adjacent location in order to service several probes.
- the sample is taken from the conditioning system to an analysis system, which consists essentially of a gas analyser (21), together with other filters, a humidity detector and a valve to control the input of samples to the analyser.
- an analysis system which consists essentially of a gas analyser (21), together with other filters, a humidity detector and a valve to control the input of samples to the analyser.
- a programmable logic controller (PLC) (22) is used to collect the analysis results, monitor the entire process and report on possible incidents. This information is sent to a control room computer (23) with the necessary user interfaces, which also collects information from other PCLs or monitoring systems.
- This computer also has software designed to offer operational recommendations to the plant operator, based on the readings, and on a number of rules gathered from experience on the optimisation of the process.
- the gases sampling probe (1) or the insertion of any sensor type into the furnace the pneumatic cylinder (15), the multiway valve (16) which controls the cylinder and other auxiliary equipment (for example, in the case of the gas sampling version, the heated filter (17), the set of control valves (18) and the sample conditioning system (19) located in the cabinet (29), which may also house the valves (16) and (18)) are all located on a motorised (25) carriage (24). This makes it possible to move the whole assembly for taking measurements in other parts of the boiler.
- the carriage (24) has several proximity sensors (26), which stop the motors at positioners (27) marking the exact position of the sampling points.
- an automated speed control (28) reduces the speed of the motors to a minimum as it approaches the positioner (27), due to a location signal provided by an appropriate device (e.g. an encoder (29) located on the carriage (24)).
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Combustion & Propulsion (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Regulation And Control Of Combustion (AREA)
- Air Supply (AREA)
Abstract
Description
- The system object of the patent consists, in its basic version, of a probe or probes and in a variety of openings, that by its special characteristics, allow the accomplishment of measurements or characterisations in high temperature areas (nearness of the burners, or any other area of the interior of the furnace of industrial boilers). These local measurements intend to optimise the operation of each burner, allowing the global improvement of parameters like combustion efficiency, loss on ignition, polluting agents formation and slagging processes.
- The small holes are drilled through the membranes which join the water tubes making up the water walls of these type of facilities, making feasible the mentioned local measurements with no need to undertake substantial modifications in the boiler. The probe is designed taking into account the limitation entailed by the membranes width (typically around 20 mm) and, therefore, the openings carried out on them.
- Additionally, the subject of this patent is the fully automated version of the described system, that allows the continuous characterisation and monitoring of boiler combustion conditions.
- These systems are equally applicable to optimisation of industrial furnaces, through the adjustment of their burners by means of measuring in areas of high temperatures.
- Industrial furnaces are facilities where the fuel (pulverised coal, fueloil, gasoil, gas, etc) is injected into the combustion chamber through burners tips, where it reaches the ignition point and bums to produce heat. This heat is transmitted to the water that circulates through the pipes that make up the boiler walls, and to other heat exchanging equipment, producing steam at high pressure and temperature. The energy of this steam may have a use in several industrial operations or it may be recovered as mechanical energy in a turbine, with the posibility to be subsequently transformed into electric energy by means of an alternator connected to the turbine.
- The performance and generation of pollutants in industrial boilers depends largely on the correct distribution of fuel and air in the furnace, and so the existence of critical areas with an inappropriate air/fuel ratio will negatively affect these extremely important parameters. In the same way, in the specific case of coal, these imbalances may generate substoichiometric areas in which the fusion point of the ash is reduced, facilitating its accumulation on the boiler tubes (slagging). This phenomenon gives rise to important heat transfer losses, and can cause problems which make it necessary to shut down the facility, with the consequent loss of production.
- These imbalances between the proportions of air and fuel are also very problematic for the burners used in the furnaces of any type of industrial process, affecting their energetic performance, as well as the quality of the products and byproducts obtained from them.
- In industrial furnaces, mainly at thermal power stations, the use of systems for the analysis of combustion gases located at the boiler outlet is frequent. These systems are used for adjusting and controlling the overall combustion process. Thus, the determination of parameters such as the oxygen and carbon monoxide at the boiler outlet, allows the identification of the correct development of the combustion.
- However, the optimisation of the process using these values has certain limitations, even when the analysis of gases is carried out at a large number of points uniformly distributed among the boiler outlets. These limitations, with respect to the distance from the actual combustion area, the evolution of the flame, and the degree of mixing of the gases in the measurement area, do not allow effective characterisation of each individual burner performance, and therefore do not permit optimisation of the overall combustion process.
- In the current state of the art, different available equips are commercialised by numerous companies (Storm Technologies, ESA, IFRF, etc), which allow direct determinations inside the furnace (water-cooled probes, suction pyrometers, high speed thermocouples, etc). However, these pieces of equipment are designed to measure through the boiler inspection ports, which are several centimetres in size and located only at certain points on the furnace.
- Therefore, this type of measurement inside the furnace is not representative enough, since it is restricted to the areas where direct access is available through the inspection ports originally installed. This restriction exists because it would require important structural modifications to the design of the boiler tube layout to make more openings of this type (over 20 mm in size, and normally around 100 mm).
- Other approaches attempt the characterisation of combustion processes consisting of systems based on sensors located on the boiler walls. These sensors measure the signals of different wavelengths produced by the combustion process itself. They can be divided into Passive Systems, which determine some property of the flames generated (such as flame detectors, infrared pyrometers, cameras or heat flow sensors located in the tubes); and Active Systems, which characterise the signals generated by emitters located in other areas of the boiler, that are attenuated or modified during their transmission through the furnace (for example, systems based on acoustic principles).
- Examples of these industrial applications based on sensors or "wall" or "contour" measurement systems are collected in numerous patents, as for example, US 4555800, US 3824391, US 4176369, DE 3224500, US 5794549, EP 0802372, DE 4328629 and US 4756684 (passive systems) and WO 9710473 (active systems), that are in any case indirect measurements of the real combustion process, since they are based on determinations taken at the edge of the furnace.
- These facts justify the little information available about the real development of the combustion processes as far as their representativeness in the boilers of industrial size is concerned.
- These limitations in the knowledge of the local combustion conditions are equally extrapolable to the furnaces of any type of industrial process.
- This invention involves a system which allows measurements to be taken in any area of the interior of the furnace of industrial boilers, specially near the burners. Some examples of this type of measurement are the evaluation of local levels of gas concentrations, temperatures, heat flows, and even image capture, in these areas of high temperature and very limited access in boilers of traditional design. The aim of these measurements is to identify the combustion conditions at any particular point inside the boilers, in order to be able to optimise heat rate, consumption of auxiliaries, and generation of pollutants and slagging.
- This local information makes it possible to consider the unit as a collection of small virtual units, each made up of a single burner. The targeted adjustment of each of these smaller units results in overall optimisation of the boiler.
- In order to meet these goals, the system allows these measurements to be made through small openings made in the membranes which join the tubes making up the water walls of the boiler. The width of these openings (around 14 mm) is limited by the width of the membranes themselves (around 20 mm), while the height is unlimited, due to the geometry of the membranes.
- This new concept for measurement inside the furnace of industrial boilers, makes it possible to place the openings in any location required, without being limited to those inspection ports included in the original design of the boiler, and permits the direct measurement of combustion conditions inside the furnace. In this way, it is possible to take measurements at the level of each burner in the boiler, without any significant structural modifications to the unit. In order to access the inside of the furnace, for the extraction of samples or the insertion of sensors, a water-cooled probe either made of or covered by ceramic material, has been specially designed for insertion through these openings, which additionally is able to withstand the high temperatures (1400 - 1700 °C) in these areas of the furnace.
- An optional upgrade to the system allows automatic operation by means of the following: motorization of the probe (insertion - extraction, lateral movement); a system of continuous treatment and analysis of the gas samples collected or of the data provided by the sensors inserted into the furnace by the probe; a cleaning system using a compressed air counterflow which guarantees the autonomy of the system between measurements; advanced monitoring software which, in addition to controlling the operation of the entire automated system and the correct processing of the results obtained, provides operational recommendations to the operator of the plant. These recommendations are based on results and the experience in the optimisation of this process.
- The invention described is applicable, to the optimisation of any type of burner, for example those in industrial furnaces.
- For a better understanding of every description contained in this report, some drawings are supplied only to serve as accomplishment examples of some system variants.
- Thus, Figure 1 presents a schematic drawing of the system in its basic version, where the sampling probe (1) is introduced through the opening (2) inside the furnace boiler (3). This small opening (2) is made in the membrane (4) which join the tubes (5) making up the water walls of the boiler, close to a facility burner.
- Figure 2 represents a probe longitudinal section (1) in its cooled and gas sampling variant; the outer socket (6) of entrance and exit of the coolant fluid and its circulation once inside the probe is shown. Also, the sample aspiration conduct can be observed (7). Figure 3 presents a front view and a cross section of the opening (2) made in the membrane (4) between the tubes (5), for the sampling probe variant (1) shown in Figure 2 (cooled and for gas sampling).
- Figure 4 presents a schematic drawing of an automated system version, specifically its variant for gas sampling, in which the sampling probes displacement can only be of insertion-extraction (a sampling probe by orifice), or with additional lateral displacement (a sampling probe for several orifices). Figure 5 shows the schematic drawing of the required elements for this variant.
- The access openings (2) are distributed throughout the boiler close to each burner. The detail of one of these openings, for the variant of cooled and gas sampling probes variant, appears in Figure 3, where its geometry can be appreciated (two semicircles of 7 mm radius joined by a square of 14 mm side).
- The water cooled probe is specially designed to support the high existing temperatures in this zone (between 1400 and 1700°C) and to accede to the interior of the boiler through the described orifices.
- In its cooled gas sampling variant (Figure 2), a tube of rectangular section can be used for its construction (14 x 12 mm sides and 1 mm thick) and two half tubes (7 mm radius and 1 mm thickness) welded as shown in the figure Section A-a. In this same section the three resulting cameras can be appreciated (8, 9, 10) through which the refrigeration fluid, for example, water, flows. Out of these, the chamber in the middle (9) is crossed by a 6 mm diameter tube through which the gas sample is extracted to be analysed. These elements are assembled at the probes end by means of two half cones and two triangular plates, according to what is observed in the detail of the probes end (Figure 2). In the opposite end an outer socket is arranged (6) allowing the exit and entrance of the refrigeration fluid and of the sample collection tube.
- Summarising, the route described by the cooling fluid is as follows: it enters through the orifice (11) into the A chamber socket (12), flowing then into the two sampling probe outer chamber (8) and (10). After reaching the end of the sampling probe the fluid returns through the central chamber (9) until reaching the B socket chamber (13) where it leaves the sampling probe through the orifice (14).
- A system automation schematic drawing is presented in Figure 4.In this figure, the sampling probe (11), being cooled or not, is coupled to a pneumatic cylinder (15), controlled by a multiway valve (16), to insert or retract the probe in or out of the furnace boiler(3).
- In the version for gas sampling and analysis, shown in the mentioned Figure 4, the sample collected by the probe passes through a heated filter to eliminate ash in suspension, and then goes to a set of valves which either send the sample to the conditioning system, or send pressurised air towards the heated filter and the probe, giving rise to a countercurrent which cleans both of these items.
- A typical sample conditioning system (19) is made up of a condenser, a cooler, a filter and a pump. This conditioning system may be housed in a cabinet (20) located on the cylinder-probe assembly support, which can also be used to house the valves, or in an adjacent location in order to service several probes.
- The sample is taken from the conditioning system to an analysis system, which consists essentially of a gas analyser (21), together with other filters, a humidity detector and a valve to control the input of samples to the analyser.
- A programmable logic controller (PLC) (22) is used to collect the analysis results, monitor the entire process and report on possible incidents. This information is sent to a control room computer (23) with the necessary user interfaces, which also collects information from other PCLs or monitoring systems. This computer also has software designed to offer operational recommendations to the plant operator, based on the readings, and on a number of rules gathered from experience on the optimisation of the process.
- This latter version has, in general, more advantages from the point of view of investment and maintenance costs, although the characterisation period is slightly increased. The photograph in Figure 9 shows this design, which is schematically presented in the plant view of the drawing in Figure 12.
- For the automated version with lateral displacement (one probe for several openings), Figure 5, the gases sampling probe (1) or the insertion of any sensor type into the furnace, the pneumatic cylinder (15), the multiway valve (16) which controls the cylinder and other auxiliary equipment (for example, in the case of the gas sampling version, the heated filter (17), the set of control valves (18) and the sample conditioning system (19) located in the cabinet (29), which may also house the valves (16) and (18)) are all located on a motorised (25) carriage (24). This makes it possible to move the whole assembly for taking measurements in other parts of the boiler.
- The carriage (24) has several proximity sensors (26), which stop the motors at positioners (27) marking the exact position of the sampling points. In order for the carriage (24) to halt exactly at the right spot, an automated speed control (28) reduces the speed of the motors to a minimum as it approaches the positioner (27), due to a location signal provided by an appropriate device (e.g. an encoder (29) located on the carriage (24)).
Claims (13)
- System which allows measurements (by means of gas extraction or by insertion of sensors) in any area of the interior of the furnace (high temperature areas) of industrial boilers (as the ones in power plants), enabling combustion process optimisation in these facilities based on the results obtained by the local measurements; this system being characterised by and comprising the following elements: A) openings to access the furnace whose reduced dimensions (width lower than the membranes which join the tubes making up the water walls of the boiler, typically <20 mm) allow their placement on the mentioned membranes, in such a way that enable direct measurements to be taken inside the boiler (not only around its surrounding area), such as gas concentration measurements by means of sampling on a prefixed point and subsequent analysis, temperature and heat flow measurements, image capture at any wavelength, without the need of carrying out structural modifications to the design of the boiler tube layout; B) small transversal dimension sampling probe or probes, specially designed for the gas sampling and sensors insertion and conditioning in high temperature areas, through the previously mentioned small openings.
- System according to claim 1, where the sampling probe or probes are inserted inside the boilers furnace through the small openings made in the proximity of each one of the burners, in order to allow their individual optimisation.
- System according to claims 1 or 2, where the sampling probe or probes are cooled by water, water with additives, oil, oil with additives, air or any other kind of coolant fluid.
- System according to claims 1 or 2, where the sampling probe or probes are constructed or externally covered by any kind of ceramic material, able to properly withstand the high temperatures existing inside the boilers furnace, avoiding in such a way the use of coolant fluids.
- System according to claims 1, 2, 3 or 4, where the sampling probe or probes are fully automated and controlled by specific software for all their various displacement capabilities, using a sampling probe provided with the insertion-extraction movement capability, for each small opening through which the measurement is intended.
- System according to claims 1, 2, 3 or 4, where the sampling probe or probes are fully automated and controlled by specific software for all their various displacement capabilities, using one or more sampling probes, each one of them used for measuring through several small openings, by means of lateral displacements in addition to the insertion-extraction movements.
- System according to claim 6, allowing the sampling probe or probes to face up the small openings to access the inside of the furnace boiler with a precision of ±1 mm, for example by the use of a combined action of proximity sensors for the final positioning at the right point, and an encoder that allows a change of speed of the lateral displacement depending on the distance to the positioner (greater speed at the beginning of the movement, and slower speed as it approaches the positioner); or by any other positioning system and determination of the sampling probe location that involves the use of infrared, acoustic, electromagnetic or any other wavelengths techniques.
- System according to claims 5, 6, or 7, characterised, in its furnace gases analysis version, by locating the treatment and conditioning systems over the sampling probe stand, moving jointly with it in the lateral displacement version described on claims 6 and 7; and being the mentioned treatment and conditioning systems composed of a dust filter to hold the ashes and a cooling and/or sample moisture condensing system.
- System according to claims 5, 6, 7, or 8, allowing the cleaning of the sampling circuit by means of countercurrent pressurised air (dust filter and sampling probe blowing) making the system autonomous between sampling periods.
- System according to claims 5, 6, 7, 8 or 9 where the results obtained in the local measurements taken by the system itself, are transferred to the facility Control Room, to enable process monitoring and adjustment.
- System according to claims 5, 6, 7, 8, 9 or 10 provided with combustion optimisation software (performance, pollutants generation, slagging, etc.) based on the results given by the system local measurements and eventually other plant operational data or results.
- System according to the previous claims applied to combustion processes other than the ones contained in claim 1, and being more specific, those which use gaseous, liquid or solid fuel or mixtures of these, under presence of air, enriched air, and in general any oxidising agent.
- System according to claims 1 to 11 applied to other industrial burners, in a global or individual way, as for example the ones mounted in process furnaces, clinker furnaces, metallurgic furnaces, toxic and dangerous waste incinerators or solid urban waste incinerators.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| ES200000355A ES2166312B1 (en) | 2000-02-16 | 2000-02-16 | SYSTEM FOR OPTIMIZATION OF COMBUSTION PROCESSES BY DIRECT MEASURES INSIDE THE HOME. |
| ES200000355 | 2000-02-16 | ||
| PCT/ES2001/000052 WO2001061297A2 (en) | 2000-02-16 | 2001-02-15 | Combustion process optimisation system by means of direct measurements inside the furnace |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1411298A2 true EP1411298A2 (en) | 2004-04-21 |
Family
ID=8492326
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20010903810 Withdrawn EP1411298A2 (en) | 2000-02-16 | 2001-02-15 | System for optimizing combustion processes by means of direct measures inside the hearth |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP1411298A2 (en) |
| AU (1) | AU2001231780A1 (en) |
| ES (1) | ES2166312B1 (en) |
| WO (1) | WO2001061297A2 (en) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2194325A1 (en) * | 2008-12-02 | 2010-06-09 | ABB Research Ltd. | Flame detection device and method for detecting a flame |
| WO2014048829A1 (en) * | 2012-09-27 | 2014-04-03 | Siemens Aktiengesellschaft | Combustion plant |
| JP2014145579A (en) * | 2013-01-23 | 2014-08-14 | Martin Gmbh Fuer Umwelt & Energietechnik | Method of running conduit in incineration plant, and device with such conduit |
| CN107807350A (en) * | 2017-09-28 | 2018-03-16 | 公安部四川消防研究所 | A kind of Experimental Calibration system and its scaling method for being used to measure vertical Light deformation amount |
| DE102024112454A1 (en) * | 2024-05-03 | 2025-11-06 | Voith Patent Gmbh | Infrared radiator, heating device and method for controlling the combustion air ratio of an infrared radiator or heating device |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ITMI20011948A1 (en) * | 2001-09-18 | 2003-03-18 | Nuovo Pignone Spa | ANTI-CONDENSATE DEVICE FOR A FLAME SENSOR OF A COMBUSTION CHAMBER |
| WO2007028840A1 (en) * | 2005-09-08 | 2007-03-15 | Ingenieria Energetica Y De Contaminacion, S.A. | System for optimising combustion in industrial ovens and boilers |
| CN114963229B (en) * | 2022-05-07 | 2024-06-04 | 吉林省电力科学研究院有限公司 | Intelligent online real-time monitoring CO combustion analysis control platform |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4514096A (en) * | 1981-11-12 | 1985-04-30 | University Of Waterloo | Furnace wall ash deposit fluent phase change monitoring system |
| JPS5944519A (en) * | 1982-09-03 | 1984-03-13 | Hitachi Ltd | Combustion condition diagnosis method |
| CH673149A5 (en) * | 1987-10-23 | 1990-02-15 | Kuepat Ag | |
| US5053978A (en) * | 1989-05-26 | 1991-10-01 | Jeffrey Solomon | Automatic boiler room equipment monitoring system |
| US5408891A (en) * | 1992-12-17 | 1995-04-25 | Beckman Instruments, Inc. | Fluid probe washing apparatus and method |
-
2000
- 2000-02-16 ES ES200000355A patent/ES2166312B1/en not_active Expired - Fee Related
-
2001
- 2001-02-15 EP EP20010903810 patent/EP1411298A2/en not_active Withdrawn
- 2001-02-15 AU AU2001231780A patent/AU2001231780A1/en not_active Abandoned
- 2001-02-15 WO PCT/ES2001/000052 patent/WO2001061297A2/en not_active Ceased
Non-Patent Citations (1)
| Title |
|---|
| See references of WO0161297A2 * |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2194325A1 (en) * | 2008-12-02 | 2010-06-09 | ABB Research Ltd. | Flame detection device and method for detecting a flame |
| WO2014048829A1 (en) * | 2012-09-27 | 2014-04-03 | Siemens Aktiengesellschaft | Combustion plant |
| JP2014145579A (en) * | 2013-01-23 | 2014-08-14 | Martin Gmbh Fuer Umwelt & Energietechnik | Method of running conduit in incineration plant, and device with such conduit |
| EP2759769A3 (en) * | 2013-01-23 | 2014-12-10 | MARTIN GmbH für Umwelt- und Energietechnik | Method for guiding a conduit in a combustion plant and device with such a conduit |
| RU2647752C2 (en) * | 2013-01-23 | 2018-03-19 | Мартин ГмбХ Фюр Умвельт-Унд Энергитехник | Method of laying a channel in the incinerator and a device having such a channel |
| CN107807350A (en) * | 2017-09-28 | 2018-03-16 | 公安部四川消防研究所 | A kind of Experimental Calibration system and its scaling method for being used to measure vertical Light deformation amount |
| CN107807350B (en) * | 2017-09-28 | 2023-08-04 | 公安部四川消防研究所 | Test calibration system for measuring vertical micro-deformation and calibration method thereof |
| DE102024112454A1 (en) * | 2024-05-03 | 2025-11-06 | Voith Patent Gmbh | Infrared radiator, heating device and method for controlling the combustion air ratio of an infrared radiator or heating device |
Also Published As
| Publication number | Publication date |
|---|---|
| WO2001061297A2 (en) | 2001-08-23 |
| ES2166312B1 (en) | 2003-04-01 |
| ES2166312A1 (en) | 2002-04-01 |
| AU2001231780A1 (en) | 2001-08-27 |
| WO2001061297A3 (en) | 2001-11-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US8584540B2 (en) | Method for measuring conditions in a power boiler furnace using a sootblower | |
| CN101398370B (en) | High temperature corrosion on-line monitoring system for boiler water-cooled wall | |
| CN101619859A (en) | Stratified combustion on-line optimization control system of boiler coal dust and optimization method thereof | |
| EP1760401A2 (en) | Method and device for monitoring the building of deposits in combustion chambers | |
| CN110398399B (en) | Flue gas extraction analysis device and boiler chamber combustion monitoring system | |
| KR101466969B1 (en) | probe unit for gathering sample gas having hydrargyrum | |
| JP7590561B2 (en) | In-situ averaging combustion oxygen analyzer | |
| WO2001061297A2 (en) | Combustion process optimisation system by means of direct measurements inside the furnace | |
| US4565561A (en) | Method of and apparatus for analyzing atmosphere of a furnace | |
| WO2012064352A1 (en) | In-line loss-on-ignition measurement system and method | |
| CN206281664U (en) | A kind of multitubular bundles integrated form radiant tube combustion experimental system | |
| JP2006226866A (en) | Exhaust gas sampling device | |
| CN214406028U (en) | A Novel Combustion System Applicable to Anti-High Temperature Corrosion of Four Corner Tangential Boiler | |
| EP3763996A1 (en) | Incineration plant for solid material | |
| CN216203287U (en) | Combustion system suitable for opposed firing boiler prevents high temperature corrosion | |
| US5365864A (en) | Laboratory scale incinerator simulation system | |
| RU2858455C1 (en) | Liquid fuel combustion test bench | |
| CN119901664A (en) | A one-dimensional furnace test system and test method for online determination of high temperature corrosion rate | |
| CN220419257U (en) | Ultralow nitrogen combustion experiment platform | |
| CN119827393A (en) | System and method for testing high-temperature corrosion rate of water-cooled wall pipe in operation | |
| McQuay et al. | The effect of rebuild on the combustion performance of an industrial gas-fired flat glass furnace | |
| Sohal | Field testing of a probe to measure fouling in an industrial flue gas stream | |
| SU1213369A1 (en) | Method of inspecting tightness of gas transfer systems | |
| FI75885B (en) | REGLERING AV PANNFUNKTIONER. | |
| SU865340A1 (en) | Contact-surface utilizer of heat of dust-ridden gases |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| 17P | Request for examination filed |
Effective date: 20030211 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): DE FR GB IT PT |
|
| R17P | Request for examination filed (corrected) |
Effective date: 20021212 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: INGENIERIA ENERGETICA Y DE CONTAMINACIO, S.A. |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20060620 |