EP1086758B1 - Verfahren und Vorrichtung zum Walzen oder Wickeln von Band - Google Patents
Verfahren und Vorrichtung zum Walzen oder Wickeln von Band Download PDFInfo
- Publication number
- EP1086758B1 EP1086758B1 EP00117879A EP00117879A EP1086758B1 EP 1086758 B1 EP1086758 B1 EP 1086758B1 EP 00117879 A EP00117879 A EP 00117879A EP 00117879 A EP00117879 A EP 00117879A EP 1086758 B1 EP1086758 B1 EP 1086758B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- band
- rollers
- rolling
- measuring roller
- section
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B37/00—Control devices or methods specially adapted for metal-rolling mills or the work produced thereby
- B21B37/48—Tension control; Compression control
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B38/00—Methods or devices for measuring, detecting or monitoring specially adapted for metal-rolling mills, e.g. position detection, inspection of the product
- B21B38/06—Methods or devices for measuring, detecting or monitoring specially adapted for metal-rolling mills, e.g. position detection, inspection of the product for measuring tension or compression
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C47/00—Winding-up, coiling or winding-off metal wire, metal band or other flexible metal material characterised by features relevant to metal processing only
- B21C47/34—Feeding or guiding devices not specially adapted to a particular type of apparatus
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C47/00—Winding-up, coiling or winding-off metal wire, metal band or other flexible metal material characterised by features relevant to metal processing only
- B21C47/34—Feeding or guiding devices not specially adapted to a particular type of apparatus
- B21C47/3408—Feeding or guiding devices not specially adapted to a particular type of apparatus for monitoring the lateral position of the material
- B21C47/3416—Feeding or guiding devices not specially adapted to a particular type of apparatus for monitoring the lateral position of the material with lateral edge contact
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C47/00—Winding-up, coiling or winding-off metal wire, metal band or other flexible metal material characterised by features relevant to metal processing only
- B21C47/34—Feeding or guiding devices not specially adapted to a particular type of apparatus
- B21C47/345—Feeding or guiding devices not specially adapted to a particular type of apparatus for monitoring the tension or advance of the material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C51/00—Measuring, gauging, indicating, counting, or marking devices specially adapted for use in the production or manipulation of material in accordance with subclasses B21B - B21F
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B15/00—Arrangements for performing additional metal-working operations specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B2015/0057—Coiling the rolled product
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B37/00—Control devices or methods specially adapted for metal-rolling mills or the work produced thereby
- B21B37/68—Camber or steering control for strip, sheets or plates, e.g. preventing meandering
Definitions
- the invention relates to a method for rolling or winding of tape with Unequal thickness over the bandwidth, in which by means of a measuring roller the Tension across the belt in one of rollers, reels, control, or pulleys limited length section of the belt is measured and takes the priority of the German patent application 199 45 202.4 on, on the content is referred to.
- Such broadband often becomes longitudinally narrower bands divided.
- These longitudinally divided bands slit strips
- These longitudinally divided bands then have at least partially a wedge-shaped cross-section, in which an edge region thicker than that other, opposite edge area is.
- Such a wedge-shaped cross section leads to difficulties in the further processing of the slit strip. This applies whenever the slit strip rolled, wound on reels or over Rollers, such as pulleys, is performed.
- the stabilizing rollers should depend on the distribution of tensile stresses on the Width of the band to be adjusted. For this purpose, the tensile stress distribution measured. Therefore, in the known device, the stabilizing rollers stored on bearing blocks, where force sensors for Determining the present in the band traction asymmetry are arranged.
- the invention is based on the object, a method and / or a device with which it is possible to obtain more accurate readings.
- the distortions when running the band caused interference voltages in the band are by means of a Shielding device kept away from the measuring roller.
- Shielding device ensures that only those tensile stresses in the area of the measuring roller occur in the band, resulting from the different length of the band about its width.
- the above-mentioned interference voltages can be Although not unavoidable with tape of uneven thickness, but with the sealing device away from the point of the tape, where the measuring roller the Tensile stress distribution in the belt measures.
- the invention also relates to a device for rolling or Wrapping tape of unequal thickness across the tape, which is a measuring roll for measuring the stresses in one of rolls, reels, control, guiding or pulleys limited length portion of the belt has.
- This device is characterized according to the invention in that between the measuring roller and an interference voltage in the band causing aggregate (Roller, reel, control, guide or deflection roller) a Abschottvortechnisch is arranged to receive the interference voltages.
- the Abschottvortechnisch is arranged between the measuring roller and that point from which the interference voltages out.
- it may be necessary second Abschottvorides use when from a second side Interference voltages to the measuring roller out can be effective.
- the measuring roller when using the Abschottsysteme actually only those voltages over the bandwidth corresponding to the length distribution of the tape and from which correct values for controlling, regulating and measuring can be derived.
- the Abschottvorraum one, preferably several rollers, which have a non-slip surface and a sufficiently large wrap angle to be in close contact with keep the tape. This close contact with the band causes an alignment effect in the belt, because the interference voltages from the belt to the rollers and their storage be transmitted and derived.
- rollers of the Abschottvoriques while adjustable, but are stored stationary during operation.
- the adjustability of Rolling allows a perfect setting of the same, especially for Ensuring the largest possible wrap angle and thus one sufficient Abschottrial.
- a solid stationary storage of roles During operation ensures a reliable derivation of the interference voltages.
- Two rollers 1 and 2 form between them a nip 3, through which a Band 4 passed, rolled and thereby reduced in thickness.
- a reel 5 is arranged, on which the Volume 4 is wound.
- a measuring roller 6 supports the band 4 from below. Not shown sensors in the measuring roller measure the forces occurring there, the give a measure of the tension in band 4.
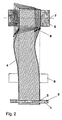
- the band 4 Since the band 4 has a wedge-shaped cross-section, it becomes on the reel wound up on its width differently tight, so that at the thicker tape position sets a higher belt tension. This leads to the belt 4 between reel 5 and measuring roller 6 is deflected to the side. This is in Fig. 2 for the purpose of a clearer representation of the consequences of the deflection a bit exaggerated.
- the unbalanced belt tension leads that the tape is bent and not with its side edges perpendicular to the reel 5 meets, that is, no longer at an angle of 90 ° to the axis of rotation 7 of the reel 5.
- This move during winding of the wedge-shaped cross-section band 4 the casserole points of the Bandes on the reel 5, and there is an asymmetrical waist geometry.
- Fig. 2 Since the band 4 has a wedge-shaped cross-section, it becomes on the reel wound up on its width differently tight, so that at the thicker tape position sets a higher belt tension. This leads to the belt 4 between reel 5 and measuring roller
- the casserole points of the band 4 are marked with arrows 8.
- Measuring roller 6 and reel 5 a completely non-uniform state of stress, at the voltages from the changing band length and the interference voltages superimposed by the unbalanced voltage introduction on Reel and distortions of the running band 4 arise.
- the Measuring roller 6 and its sensors can not between the two types of voltage differ. Consequently, the measured values thus obtained are useless.
- FIG. 3 also shows a device for rolling a strip 4, which is wound by a reel 5. It is immaterial if the There existing measuring roller 6 is arranged above the belt 4. She works on the same principle as the measuring roller 6 in Figs. 1, 2. Crucial However, that in Fig. 3 between the measuring roller 6 and the reel 5 a Abschottvoriques 9 is arranged. This consists of a roll 10 with a sufficient non-slip surface. The roller 10 should also be arranged so that there is a sufficiently large wrap angle and thus the band 4 has a large-area contact with the roller 10. The role 10 could be around this to reach, also be adjustable. During operation, their location remains however stationary and stable to absorb and dissipate the disturbing voltages, which act from the reel 5 ago against the direction of the tape 4 in the band.
- Fig. 3 is still a plan view of the tape 4, in which the forces are shown as arrows.
- the forces are shown as arrows.
- Far left If one recognizes the unequal forces immediately at the emergence of the band 4 the reel 5 at the point marked 11. In the middle area are represented the forces acting at the point 12 in the band 4.
- On the far right is shown that in the region of the measuring roller 6, for example at the point 13, only the Forces occur, resulting from the length distribution of the strip across the width arise because the noise coming from the reel 5 ago the Abschottvortechnisch 9 do not happen as they are derived.
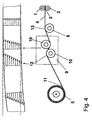
- FIG. 4 differs from FIG. 3 mainly in that there is a Shielding device 9 is shown, which has two rollers 10. In this way can be an even larger wrap angle in total and thus still achieve more reliable isolation of the interference voltages. Abschottvoriquesen with more than two rolls 10 are quite possible and in some cases also useful and necessary.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Force Measurement Appropriate To Specific Purposes (AREA)
- Measurement Of Length, Angles, Or The Like Using Electric Or Magnetic Means (AREA)
- Controlling Rewinding, Feeding, Winding, Or Abnormalities Of Webs (AREA)
- Control Of Metal Rolling (AREA)
Description
- Fig. 1:
- eine bekannte Vorrichtung zum Walzen von Band in schematischer Darstellung in einer Seitenansicht;
- Fig. 2:
- die Vorrichtung nach Fig. 1 in größerem Maßstab in der Draufsicht;
- Fig. 3:
- eine erfindungsgemäße Vorrichtung mit einer einrolligen Abschottung und
- Fig. 4:
- eine erfindungsgemäße Vorrichtung mit einer doppelrolligen Abschottung.
Claims (4)
- Verfahren zum Walzen oder Wickeln von im Querschnitt keilförmigem Band mit ungleicher Dicke über die Bandbreite, bei dem ein Randbereich dicker als der andere, gegenüberliegende Randbereich ist, bei dem mittels einer Messrolle die Spannung in einem von Walzen, Haspeln, Steuer-, Führungs- oder Umlenkrollen begrenzten Längenabschnitt des Bandes gemessen wird, dadurch gekennzeichnet, dass durch unsymmetrische Spannungseinleitung und durch Verzerrungen beim Verlaufen des Bandes (4) im Band verursachte Störspannungen mittels einer Abschottvorrichtung (9) von der Messrolle (6) ferngehalten werden.
- Vorrichtung zum Walzen oder Wickeln von im Querschnitt keilförmigem Band, bei dem ein Randbereich dicker als der andere, gegenüberliegende Randbereich ist, mit einer Messrolle zum Messen der Spannungen in einem von Walzen, Haspeln, Steuer-, Führungs- oder Umlenkrollen begrenzten Längenabschnitt des Bandes, dadurch gekennzeichnet, dass zwischen der Messrolle (6) und einem Störspannungen im Band (4) verursachenden Aggregat (5) eine Abschottvorrichtung (9) zur Aufnahme der Störspannungen angeordnet ist.
- Vorrichtung nach Anspruch 2, dadurch gekennzeichnet, dass die Abschottvorrichtung (9) mindestens eine Rolle (10) besitzt.
- Vorrichtung nach Anspruch 3, dadurch gekennzeichnet, dass die Rollen (10) verstellbar, jedoch während des Betriebes ortsfest gelagert sind.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19945202 | 1999-09-21 | ||
| DE19945202A DE19945202A1 (de) | 1999-09-21 | 1999-09-21 | Verfahren und Vorrichtung zum Walzen oder Wickeln von Band |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1086758A2 EP1086758A2 (de) | 2001-03-28 |
| EP1086758A3 EP1086758A3 (de) | 2003-09-10 |
| EP1086758B1 true EP1086758B1 (de) | 2005-10-26 |
Family
ID=7922764
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP00117879A Expired - Lifetime EP1086758B1 (de) | 1999-09-21 | 2000-08-19 | Verfahren und Vorrichtung zum Walzen oder Wickeln von Band |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US6840475B1 (de) |
| EP (1) | EP1086758B1 (de) |
| JP (1) | JP2001105025A (de) |
| DE (2) | DE19945202A1 (de) |
| ES (1) | ES2251919T3 (de) |
Families Citing this family (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10133756A1 (de) * | 2001-07-11 | 2003-01-30 | Sms Demag Ag | Kaltwalzwerk sowie Verfahren zum Kaltwalzen von metallischem Band |
| DE102004041321A1 (de) * | 2004-08-26 | 2006-03-02 | Sms Demag Ag | Walzwerk zum Walzen von metallischem Band |
| DE102004043150A1 (de) * | 2004-09-03 | 2006-03-09 | Betriebsforschungsinstitut VDEh - Institut für angewandte Forschung GmbH | Spannrolle für eine Bandbehandlungsanlage sowie Bandbehandlungsanlage und Verwendung der Spannrolle |
| US8032246B2 (en) * | 2007-02-02 | 2011-10-04 | Kimberly-Clark Worldwide, Inc. | Winding method for uniform properties |
| CN101623720B (zh) * | 2008-07-09 | 2011-11-16 | 上海格林赛高新材料有限公司 | 控制异型金属带带型的卷取装置 |
| US8707529B2 (en) * | 2008-12-11 | 2014-04-29 | The Material Works, Ltd. | Method and apparatus for breaking scale from sheet metal with recoiler tension and rollers adapted to generate scale breaking wrap angles |
| US20130193249A1 (en) * | 2012-01-31 | 2013-08-01 | Georgia-Pacific Consumer Products Lp | Product, Dispenser and Method of Dispensing Product |
| CN103170524B (zh) * | 2013-03-18 | 2014-12-10 | 中冶南方(武汉)自动化有限公司 | 冷连轧生产线转盘式高速卷取机控制方法及系统 |
| CN104084448B (zh) * | 2014-06-16 | 2016-03-16 | 中国重型机械研究院股份公司 | 一种用于重卷剖分机组双卷取机的同步控制系统 |
| CN117161132A (zh) * | 2023-09-18 | 2023-12-05 | 太原科技大学 | 一种全电动伺服控制金属极薄带材拉伸弯曲矫直机组 |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1958692A (en) * | 1930-09-11 | 1934-05-15 | United States Gypsum Co | Sheet handling machine |
| US2433014A (en) * | 1943-03-31 | 1947-12-23 | Carnegie Illinois Steel Corp | Apparatus for handling metallic strip |
| US3268142A (en) * | 1964-03-12 | 1966-08-23 | Macomson Wistar Wright | Web tensioner and spreader |
| US3227347A (en) * | 1964-03-31 | 1966-01-04 | Wean Engineering Co Inc | Apparatus for controlling the tension in a strip advancing continuously in a strip processing line |
| US3330457A (en) * | 1965-02-11 | 1967-07-11 | Mount Hope Machinery Ltd | Total tension monitor and control system |
| US4339934A (en) * | 1980-11-28 | 1982-07-20 | Reynolds Metals Company | Strip shape control |
| US4478062A (en) * | 1982-09-01 | 1984-10-23 | E. W. Bliss Company, Inc. | Strip shape measuring roll |
| US4463586A (en) * | 1983-04-13 | 1984-08-07 | Reycan Research Limited | Auto wrap angle/positioner for shape sensing roll |
| JPH0299211A (ja) * | 1988-10-06 | 1990-04-11 | Mitsubishi Electric Corp | 圧延材の板形状制御装置 |
| DE69209609T2 (de) * | 1991-05-03 | 1996-10-31 | Eastman Kodak Co | Steuerung für das aufwickeln von bahnen |
| SE507318C2 (sv) * | 1994-11-23 | 1998-05-11 | Moelnlycke Ab | Aggregat för att reglera utgående spänning i en materialbana |
| DE19524729A1 (de) * | 1995-07-07 | 1997-01-16 | Sundwiger Eisen Maschinen | Verfahren und Vorrichtung zum Walzen von Bändern mit über ihrer Breite ungleichförmige Dicken- und/oder Längenverteilung |
-
1999
- 1999-09-21 DE DE19945202A patent/DE19945202A1/de not_active Withdrawn
-
2000
- 2000-08-19 ES ES00117879T patent/ES2251919T3/es not_active Expired - Lifetime
- 2000-08-19 EP EP00117879A patent/EP1086758B1/de not_active Expired - Lifetime
- 2000-08-19 DE DE50011425T patent/DE50011425D1/de not_active Expired - Lifetime
- 2000-09-20 JP JP2000286179A patent/JP2001105025A/ja active Pending
- 2000-09-20 US US09/666,867 patent/US6840475B1/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| ES2251919T3 (es) | 2006-05-16 |
| US6840475B1 (en) | 2005-01-11 |
| EP1086758A2 (de) | 2001-03-28 |
| DE19945202A1 (de) | 2001-03-22 |
| DE50011425D1 (de) | 2005-12-01 |
| EP1086758A3 (de) | 2003-09-10 |
| JP2001105025A (ja) | 2001-04-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE102007006810B3 (de) | Vorrichtung zum Planieren von Metallbändern | |
| DE2334492A1 (de) | Steuergeraet fuer walzgerueste | |
| DE3115461C2 (de) | ||
| DE19520541C2 (de) | Verfahren und Vorrichtung zum Korrigieren eines gewalzten, in der Bandebene horizontal gebogenen Metallbandes, insbesondere eines Metallbandes mit einer Banddicke von 0,5 mm bis 2,0 mm | |
| EP0393519A2 (de) | Vorrichtung zum Aufwickeln einer Folienbahn | |
| CH647476A5 (de) | Transportvorrichtung fuer blattgut. | |
| EP1086758A2 (de) | Verfahren und Vorrichtung zum Walzen oder Wickeln von Band | |
| DE4323385C1 (de) | Verfahren zum Beseitigen von Querkrümmungen in Metallbändern, insbesondere dünnen Metallbändern bis 2,0 mm Dicke | |
| DE3036794C2 (de) | Fördervorrichtung für Band- und Folienmaterial für Bandbearbeitungsmaschinen | |
| DE19524729A1 (de) | Verfahren und Vorrichtung zum Walzen von Bändern mit über ihrer Breite ungleichförmige Dicken- und/oder Längenverteilung | |
| DE3545270C1 (de) | Breitstreckvorrichtung | |
| DE69901667T2 (de) | Einwickelvorrichtung | |
| EP1789211B1 (de) | Bandbehandlungsanlage und verwendung einer spannrolle in einer bandbehandlungsanlage | |
| DE4419662A1 (de) | Wickelmaschine zum Aufwickeln einer laufenden Papierbahn | |
| EP0603598A1 (de) | Verfahren zum Herstellen eines Stahlbandes durch Giessen eines Stranges und anschliessendes Walzen | |
| DE3413969A1 (de) | Stuetzrolle(n) fuer eine vorrichtung zum geraderichten zylindrischer werkstuecke | |
| DE102018127037B4 (de) | Kalander | |
| EP4005695B1 (de) | Spannrollensatz für eine richtanlage zum richten eines bandes, richtanlage, nachwalzgerüstanlage und verfahren zum betreiben einer richtanlage | |
| DE19535632C2 (de) | Vorrichtung zur Verhinderung von Registerabweichungen beim Bedrucken einer in einer Rotationsdruckmaschine laufenden Bedruckstoffbahn | |
| EP1873099B1 (de) | Walze zum Führen und Breitstrecken von Bandmaterial | |
| EP1514816B1 (de) | Wickelmaschine zum Wickeln einer Materialbahn | |
| DE10128576A1 (de) | Verfahren und Vorrichtung zum Umlenken von Bändern | |
| DE19734831A1 (de) | Tragwalzen-Wickelvorrichtung | |
| DE8708849U1 (de) | Doppeltragwalzen-Wickelmaschine | |
| DE3537018A1 (de) | Zugzylinder bei einer rotationsdruckmaschine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: 7B 21C 47/34 B Ipc: 7B 21B 38/06 A Ipc: 7B 21B 37/48 B Ipc: 7B 21C 51/00 B |
|
| 17P | Request for examination filed |
Effective date: 20040305 |
|
| AKX | Designation fees paid |
Designated state(s): AT DE ES FR IT SE |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): DE ES FR GB IT SE |
|
| 17Q | First examination report despatched |
Effective date: 20040913 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: BETRIESFORSCHUNGSINSTITUT VDEHINSTITUT FUER ANGEWA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: BETRIEBSFORSCHUNGSINSTITUT VDEHINSTITUT FUER ANGEW |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT SE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REF | Corresponds to: |
Ref document number: 50011425 Country of ref document: DE Date of ref document: 20051201 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20060119 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2251919 Country of ref document: ES Kind code of ref document: T3 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20060727 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20090821 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20090821 Year of fee payment: 10 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20100819 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100819 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20111019 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100820 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 18 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20190821 Year of fee payment: 20 Ref country code: FR Payment date: 20190822 Year of fee payment: 20 Ref country code: SE Payment date: 20190826 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20190923 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |