EP1042746B1 - Procede de fabrication de noyaux d'identite pour des sceaux a ultrasons - Google Patents
Procede de fabrication de noyaux d'identite pour des sceaux a ultrasons Download PDFInfo
- Publication number
- EP1042746B1 EP1042746B1 EP98965862A EP98965862A EP1042746B1 EP 1042746 B1 EP1042746 B1 EP 1042746B1 EP 98965862 A EP98965862 A EP 98965862A EP 98965862 A EP98965862 A EP 98965862A EP 1042746 B1 EP1042746 B1 EP 1042746B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- identity
- integrity
- stack
- core
- disks
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 9
- 238000002604 ultrasonography Methods 0.000 title claims abstract description 5
- 239000002184 metal Substances 0.000 claims abstract description 11
- 238000005476 soldering Methods 0.000 claims description 9
- 238000004519 manufacturing process Methods 0.000 claims description 7
- 230000008030 elimination Effects 0.000 claims 1
- 238000003379 elimination reaction Methods 0.000 claims 1
- 238000005219 brazing Methods 0.000 abstract description 11
- 239000011324 bead Substances 0.000 abstract 1
- 229910000679 solder Inorganic materials 0.000 description 9
- 238000005520 cutting process Methods 0.000 description 5
- 239000008188 pellet Substances 0.000 description 3
- 238000002592 echocardiography Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 238000004080 punching Methods 0.000 description 2
- 238000009736 wetting Methods 0.000 description 2
- 230000000694 effects Effects 0.000 description 1
- 239000000383 hazardous chemical Substances 0.000 description 1
- 238000010348 incorporation Methods 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000005259 measurement Methods 0.000 description 1
- 239000002245 particle Substances 0.000 description 1
- 230000002285 radioactive effect Effects 0.000 description 1
- 239000012857 radioactive material Substances 0.000 description 1
- 239000002901 radioactive waste Substances 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 238000010408 sweeping Methods 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
Images

Classifications
-
- G—PHYSICS
- G09—EDUCATION; CRYPTOGRAPHY; DISPLAY; ADVERTISING; SEALS
- G09F—DISPLAYING; ADVERTISING; SIGNS; LABELS OR NAME-PLATES; SEALS
- G09F3/00—Labels, tag tickets, or similar identification or indication means; Seals; Postage or like stamps
- G09F3/02—Forms or constructions
- G09F3/03—Forms or constructions of security seals
- G09F3/0305—Forms or constructions of security seals characterised by the type of seal used
- G09F3/0317—Forms or constructions of security seals characterised by the type of seal used having bolt like sealing means
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49826—Assembling or joining
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49826—Assembling or joining
- Y10T29/49904—Assembling a subassembly, then assembling with a second subassembly
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49826—Assembling or joining
- Y10T29/49947—Assembling or joining by applying separate fastener
- Y10T29/49966—Assembling or joining by applying separate fastener with supplemental joining
- Y10T29/49968—Metal fusion joining
Definitions
- the present invention relates to a method of manufacture of identity cores for seals ultrasonic, each core comprising a brazed stack of discs with at least one notch, the identity being defined at least in part by the angular position random of the different notches in the disc stack.
- any transport or storage of radioactive materials must be constantly monitored by international inspectors. To accomplish their mission, the inspectors must be able to seal containers and verify the seals with regard to their identity and integrity.
- identity kernels by stacking a certain number of discs slotted so that once the battery suitably assembled by soldering, the identity is defined at least in part by the random position of notches in the stack, so cavities which, thanks to the brazing, become the seat of ultrasonic echoes. Identity is thus created by soldering into a single block of a random assembly of discs, presenting themselves a random nature in their manufacture individual.
- nuclei are optionally combined with a rod of integrity which includes a privileged rupture zone in violation of this integrity.
- a ultrasonic reader on a bolt incorporating such a core, so we can record the ultrasonic response corresponding, on the one hand, to the identity of this seal and, on the other hand, at the level of the integrity rod, to the integrity of the bolt.
- the present invention relates to the manufacturing process identity kernels that can adapt to such seals or others. It has been found that the individual core fabrication is complex with a view to large number required (new kernel required after each unscrewing) and small dimensions of the cores (diameter 12mm, height 5mm) and in particular for the requirements of quality. We must for example ensure absolute flatness discs whose thickness hardly exceeds one millimeter.
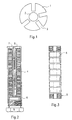
- Figure 1 shows a view of a disc making part of the core manufactured according to the invention.
- Figure 2 shows an axial section of a stack of discs prepared for brazing within the process according to the invention.
- FIG. 3 shows a step following brazing, namely the cutting of the stack into individual pellets.
- Figure 4 shows a top view of such pellet modified to be associated with an integrity rod.
- Figure 5 shows in section the association of a nucleus modified according to FIG. 4 and an integrity rod during soldering of these two elements.
- each disc 1 of general shape circular with a thickness of 1 mm has a central hole 2 with a diameter of 3.6 mm and laterally at least one notch 3 which extends from the periphery radially towards the near the perimeter of the central hole 2.
- the width of this notch is for example 1.5 mm.
- Such discs can be made by punching in large series. However, these discs must be perfectly flat and free of burrs.
- the number of identity cores would be limited. If we wants to increase this number with constant measurement quality we can provide two, three or even four notches and / or vary the thickness of the discs, the different types of discs then being combined randomly.
- the angle between two neighboring notches should be enough so as not to weaken the mechanical stability of the discs too much, by example greater than 40 °, preferably greater than 60 °.
- nuclei will be composed of discs of thickness varying from 0.9 to 1.3 mm, but the invention is not limited to this case.
- the sleeve has at one end a hole 5 and it can be closed at the other end by a plug threaded 6.
- the dimensions of this sleeve 4 are chosen from so that we can fill its interior volume with a given number of discs, for example 50, and that this stack can be compressed by tightening the cap 6.
- the sheath thus filled with a compressed pile of discs and a solder bar is then introduced in an oven.
- the interior of this oven can be evacuated and / or placed under an inert atmosphere.
- temperature rise and fall can be programmed as required.
- the solder When soldering, the solder penetrates by wetting in all metal-metal interfaces and wets all walls, including those of the cavities formed by the notches 3 of the discs. Possibly a small amount of solder can agglutinate a residual particle at the wall, thus causing another random factor.
- the discs When the soldering is finished, the discs are welded to each other in a random angular position and constitute a block compact.
- Figure 3 shows this column in axial section after cutting into nine tablets such as the tablet 8.
- the height of each tablet is 5.2 mm.
- the plans of sectioning are located randomly in relation to the interface between two neighboring disks.
- Each tablet has an own identity which mainly depends on the position angle of the metal discs which compose it and which can be read by an ultrasonic reader scanning a circular trace of intermediate diameter between that of central hole 2 of the discs and the periphery of the patch.
- a patch associated with a delay line 13 (see fig. 5) will it constitute a nucleus of identity can be incorporated by mounting or welding into a bolt security that can be used, for example, for closing guarantee of a radioactive waste container, the random structure of the nucleus protecting it from copying.
- Integrity rod 10 is an extension of the block solid metal 13 which will constitute a delay line crossed by ultrasound once joined by brazing to the 8 'identity tag.
- Integrity rod 10 is provided of a weakened section 11 of privileged rupture likely to be broken by pulling, twisting or shear (or a combination of these effects). She will be connected in the final assembly by its anchor tail 12 to a mechanical element (not shown) inside the bolt to protect.
- Block 13 (delay line), with its integrity rod 10, is placed in a brazing sheath 14 similar to the brazing sleeve 4.
- the plug 15 of this sheath has a central cavity 16 for accommodating a solder bar, and it can be screwed into the sheath to compress block 13 and the underlying identity patch 8 or 8 '.
- the whole is brazed according to a method similar to that described using Figure 2.
- the solder no longer enters the stack but simply secures the 8 or 8 'pad and the block 13 with the sheath 14.
- the places wetted by the solder are marked with a bold line 17.
- the last step in the production of this core combined identification and integrity is to separate the head of the sheath with the plug 15 of the rest by cutting perpendicular to the axis of the nucleus along a line 18 at the upper level of block 13 corresponding to the exact thickness desired for the delay line.
- parts which have become useless of the sheath 14 will be removed, on the one hand, by sectioning along a line 19 perpendicular to the axis, at the lower level of the patch 8 ', and, on the other hand, by turning along a cylinder 20 leaving a sheath about 1 mm thick around the assembly formed by the block 13 and the pad 8 '.
- the face of identity reading and the integrity state of the seal is then constituted by the sectioning surface.
- the identity kernel can be used alone for simply unequivocally define the identity of an object to which it would be associated or incorporated.
Landscapes
- Engineering & Computer Science (AREA)
- Computer Security & Cryptography (AREA)
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Theoretical Computer Science (AREA)
- Lining Or Joining Of Plastics Or The Like (AREA)
- Powder Metallurgy (AREA)
- Package Closures (AREA)
- Monitoring And Testing Of Nuclear Reactors (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
- Steroid Compounds (AREA)
- Transducers For Ultrasonic Waves (AREA)
- Pressure Welding/Diffusion-Bonding (AREA)
- Medicinal Preparation (AREA)
- Investigating Or Analyzing Materials By The Use Of Ultrasonic Waves (AREA)
- Adornments (AREA)
- Packaging For Recording Disks (AREA)
Description
Claims (4)
- Procédé de fabrication de noyaux d'identité pour des sceaux à ultrasons, chaque noyau étant constitué d'une ligne à retard (13) et d'une pile brasée de disques métalliques (1) portant au moins une encoche (3), l'identité étant définie par la position angulaire aléatoire des différentes encoches dans la pile, caractérisé en ce quedes disques (1) encochées et munies d'un trou central (2) sont d'abord empilées en grand nombre dans un fourreau métallique tubulaire (4) de section intérieure circulaire correspondant aux dits disques (1),on comprime axialement l'empilement dans le fourreau (4) et on introduit une barrette de brasure (7) dans le canal constitué par l'ensemble des trous centraux alignés (2),on effectue un brasage dans un four à vide,après élimination des deux extrémités du fourreau on sectionne la colonne ainsi obtenue perpendiculairement à son axe en une pluralité de pastilles d'identité individuelles (8) d'épaisseur prédéterminée,enfin on obtient ledit noyau en associant par brasage un bloc métallique (13) servant de ligne à retard à une telle pastille (8, 8').
- Procédé selon la revendication 1, caractérisé en ce que les encoches (3) ont une forme allongée et s'étendent radialement de la périphérie du disque (1) vers un diamètre légèrement supérieur à celui du trou central (2).
- Procédé selon la revendication 2, caractérisé en ce que, le nombre d'encoches (3) par disque (1) excédant un, l'angle entre deux encoches voisines est supérieur ou égal à 40°, et de préférence supérieur ou égal à 60°.
- Noyau d'identité fabriqué par le procédé selon l'une des revendications précédentes, caractérisé en ce que, faisant partie d'un ensemble brasé d'identité et d'intégrité, il comporte une encoche supplémentaire (9) réalisée après le brasage de l'empilement et s'étendant sur toute son épaisseur, pour laisser passer une tige d'intégrité (10) qui fait partie du bloc métallique (13) et qui présente une zone de rupture privilégiée (11) pour le cas d'une violation de l'intégrité, cette violation étant détectable par ultrasons lors de la lecture de l'identité du noyau.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| LU90187 | 1997-12-22 | ||
| LU90187A LU90187B1 (fr) | 1997-12-22 | 1997-12-22 | Procédé de fabrication de noyaux d'identité pour des sceaux à ultrasons |
| PCT/EP1998/008385 WO1999033045A1 (fr) | 1997-12-22 | 1998-12-21 | Procede de fabrication de noyaux d'identite pour des sceaux a ultrasons |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1042746A1 EP1042746A1 (fr) | 2000-10-11 |
| EP1042746B1 true EP1042746B1 (fr) | 2002-03-06 |
Family
ID=19731727
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98965862A Expired - Lifetime EP1042746B1 (fr) | 1997-12-22 | 1998-12-21 | Procede de fabrication de noyaux d'identite pour des sceaux a ultrasons |
Country Status (12)
| Country | Link |
|---|---|
| US (1) | US6694593B1 (fr) |
| EP (1) | EP1042746B1 (fr) |
| JP (1) | JP2001527219A (fr) |
| AT (1) | ATE214186T1 (fr) |
| CA (1) | CA2310134C (fr) |
| DE (1) | DE69804140T2 (fr) |
| DK (1) | DK1042746T3 (fr) |
| ES (1) | ES2174541T3 (fr) |
| LU (1) | LU90187B1 (fr) |
| NO (1) | NO315178B1 (fr) |
| PT (1) | PT1042746E (fr) |
| WO (1) | WO1999033045A1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11410578B2 (en) | 2016-02-15 | 2022-08-09 | The European Atomic Energy Community (Euratom), Represented By The European Commission | Sealing bolt and method of installing a sealing bolt |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1798426A1 (fr) * | 2005-12-13 | 2007-06-20 | The European Community, represented by the European Commission | Serrage d'un boulon |
| EP1826422A1 (fr) | 2006-02-23 | 2007-08-29 | The European Community, represented by the European Commission | Boulons de scellement |
| EP3205996A1 (fr) | 2016-02-15 | 2017-08-16 | The European Atomic Energy Community (EURATOM), represented by the European Commission | Système et procédé de prévention de fraude pour processus d'inviolabilité |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| LU83337A1 (de) * | 1981-05-05 | 1983-03-24 | Euratom | Multimarkierungssiegel |
| US5228250A (en) * | 1992-08-03 | 1993-07-20 | Kesselman David A | Tamper proof anchor bolt assembly |
| GB9218666D0 (en) * | 1992-09-03 | 1992-10-21 | Euratom | Ultrasonic sealing bolts and identification bolts |
| US5807048A (en) * | 1992-09-03 | 1998-09-15 | European Atomic Energy Community (Euratom) | Sealing fastener with ultrasonic identifier and removal attempt indicator, and ultrasonic reading device for same |
-
1997
- 1997-12-22 LU LU90187A patent/LU90187B1/fr active
-
1998
- 1998-12-21 CA CA002310134A patent/CA2310134C/fr not_active Expired - Fee Related
- 1998-12-21 US US09/530,354 patent/US6694593B1/en not_active Expired - Lifetime
- 1998-12-21 DE DE69804140T patent/DE69804140T2/de not_active Expired - Lifetime
- 1998-12-21 EP EP98965862A patent/EP1042746B1/fr not_active Expired - Lifetime
- 1998-12-21 JP JP2000525876A patent/JP2001527219A/ja not_active Withdrawn
- 1998-12-21 DK DK98965862T patent/DK1042746T3/da active
- 1998-12-21 AT AT98965862T patent/ATE214186T1/de active
- 1998-12-21 ES ES98965862T patent/ES2174541T3/es not_active Expired - Lifetime
- 1998-12-21 PT PT98965862T patent/PT1042746E/pt unknown
- 1998-12-21 WO PCT/EP1998/008385 patent/WO1999033045A1/fr not_active Ceased
-
2000
- 2000-03-14 NO NO20001321A patent/NO315178B1/no not_active IP Right Cessation
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11410578B2 (en) | 2016-02-15 | 2022-08-09 | The European Atomic Energy Community (Euratom), Represented By The European Commission | Sealing bolt and method of installing a sealing bolt |
Also Published As
| Publication number | Publication date |
|---|---|
| DE69804140D1 (de) | 2002-04-11 |
| NO20001321L (no) | 2000-06-22 |
| CA2310134C (fr) | 2008-02-12 |
| PT1042746E (pt) | 2002-07-31 |
| DK1042746T3 (da) | 2002-06-24 |
| DE69804140T2 (de) | 2002-07-25 |
| LU90187B1 (fr) | 1999-06-24 |
| US6694593B1 (en) | 2004-02-24 |
| WO1999033045A1 (fr) | 1999-07-01 |
| NO315178B1 (no) | 2003-07-21 |
| JP2001527219A (ja) | 2001-12-25 |
| ES2174541T3 (es) | 2002-11-01 |
| EP1042746A1 (fr) | 2000-10-11 |
| CA2310134A1 (fr) | 1999-07-01 |
| ATE214186T1 (de) | 2002-03-15 |
| NO20001321D0 (no) | 2000-03-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2585882B1 (fr) | Systeme antichoc de piece d'horlogerie | |
| EP2140459B1 (fr) | Emballage pour le transport et/ou stockage de matieres nucleaires comprenant une protection radiologique en plomb coule sur une armature metallique | |
| EP2904613B1 (fr) | Emballage pour le transport et/ou l'entreposage de matieres radioactives, comprenant des moyens ameliores de fixation d'un capot amortisseur de chocs | |
| FR2864322A1 (fr) | Crayon de combustible pour un reacteur nucleaire | |
| FR2891165A1 (fr) | Ensemble de conditionnement d'un volume predetermine de substance a conserver par vitrification cryogenique. | |
| EP3042379B1 (fr) | Élément de protection amortisseur pour un emballage de transport et/ou entreposage de matières radioactives | |
| FR2715807A1 (fr) | Procédé de fabrication de pièces monétaires, de médailles ou de jetons notamment bimétalliques, pièces, médailles ou jetons obtenus et couronne et insert pour leur fabrication. | |
| CA2310134C (fr) | Procede de fabrication de noyaux d'identite pour des sceaux a ultrasons | |
| EP1928601B1 (fr) | Ensemble de conditionnement d'un volume predetermine de substance biologique destinee a etre plongee dans un agent cryogenique liquide | |
| EP1005049A1 (fr) | Dispositif amortisseur de chocs pour conteneurs de matières radioactives | |
| EP4073822B1 (fr) | Dispositif de rangement pour l'entreposage et/ou le transport d'assemblages de combustible nucleaire, présentant une conception à coûts réduits | |
| FR3054922A1 (fr) | Panier de rangement pour matieres radioactives, presentant un encombrement optimise | |
| EP1525591B1 (fr) | Paroi de protection a blindage anti-poincon pour conteneur et conteneur comprenant au moins une telle paroi | |
| EP1576621B1 (fr) | Conteneur pour le stockage/transport de matieres radioactives non irradiees telles que des assemblages de combustible nucleaire | |
| EP0341139B1 (fr) | Procédé de conditionnement de déchets radioactifs et dispositifs pour le mettre en oeuvre | |
| EP4239155B1 (fr) | Structure de sécurité renforcée | |
| EP4315369B1 (fr) | Ensemble pour le transport d'hexafluorure d'uranium, comprenant des capots amortisseurs de choc | |
| FR2733316A1 (fr) | Muratisation par dilatation differentielle | |
| FR3109240A1 (fr) | Dispositif de rangement pour l’entreposage et/ou le transport d’assemblages de combustible nucleaire, presentant une conception a couts reduits | |
| FR3094704A1 (fr) | Plot de guidage à déformation contrôlée pour structure destinée au chargement/déchargement d’un emballage, notamment de transport et/ou d’entreposage de matières radioactives | |
| EP4309190A1 (fr) | Traversée de ventilation pour une paroi radio-protectrice et la paroi radio-protectrice équipée | |
| FR2622039A1 (fr) | Crayon combustible a surete amelioree et procede de realisation d'un bouchon utilisable dans un tel crayon | |
| FR3121265A1 (fr) | Ensemble pour le transport d’hexafluorure d’uranium | |
| FR3107200A1 (fr) | Installation pour la fabrication de contenants en aluminium ou en alliage d’aluminium apte à créer des dissymétries axiales de rigidification dans le contenant après traitement thermique |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20000511 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 20010530 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| REF | Corresponds to: |
Ref document number: 214186 Country of ref document: AT Date of ref document: 20020315 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 69804140 Country of ref document: DE Date of ref document: 20020411 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20020521 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20020507 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20020402198 Country of ref document: GR |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2174541 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20021209 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: MC Payment date: 20031124 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DK Payment date: 20031125 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PT Payment date: 20031127 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20031128 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GR Payment date: 20031202 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041221 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050621 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050704 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MM4A Effective date: 20050621 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD Ref country code: FR Ref legal event code: CA |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 69804140 Country of ref document: DE Owner name: EUROPEAN UNION, BE Free format text: FORMER OWNER: EUROPEAN COMMUNITY, BRUSSELS, BE Effective date: 20110208 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20151119 Year of fee payment: 18 Ref country code: DE Payment date: 20151119 Year of fee payment: 18 Ref country code: FI Payment date: 20151120 Year of fee payment: 18 Ref country code: IT Payment date: 20151120 Year of fee payment: 18 Ref country code: LU Payment date: 20151123 Year of fee payment: 18 Ref country code: GB Payment date: 20151125 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20151119 Year of fee payment: 18 Ref country code: FR Payment date: 20151123 Year of fee payment: 18 Ref country code: AT Payment date: 20151120 Year of fee payment: 18 Ref country code: ES Payment date: 20151204 Year of fee payment: 18 Ref country code: SE Payment date: 20151124 Year of fee payment: 18 Ref country code: BE Payment date: 20151123 Year of fee payment: 18 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161231 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69804140 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161221 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20170101 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 214186 Country of ref document: AT Kind code of ref document: T Effective date: 20161221 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20161221 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170101 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20170831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161221 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161221 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161221 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170102 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161231 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170701 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161221 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20161231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020306 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20180628 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161222 |
|
| RIC2 | Information provided on ipc code assigned after grant |
Ipc: G09F 3/03 20060101AFI19990715BHEP |