EP0972621B1 - Verfahren zur Herstellung poriger Pasten, insbesondere porigem Gipsbrei und Mischer - Google Patents
Verfahren zur Herstellung poriger Pasten, insbesondere porigem Gipsbrei und Mischer Download PDFInfo
- Publication number
- EP0972621B1 EP0972621B1 EP99110837A EP99110837A EP0972621B1 EP 0972621 B1 EP0972621 B1 EP 0972621B1 EP 99110837 A EP99110837 A EP 99110837A EP 99110837 A EP99110837 A EP 99110837A EP 0972621 B1 EP0972621 B1 EP 0972621B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- mixing
- gypsum
- fine
- mixer
- porous
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28C—PREPARING CLAY; PRODUCING MIXTURES CONTAINING CLAY OR CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28C5/00—Apparatus or methods for producing mixtures of cement with other substances, e.g. slurries, mortars, porous or fibrous compositions
- B28C5/38—Apparatus or methods for producing mixtures of cement with other substances, e.g. slurries, mortars, porous or fibrous compositions wherein the mixing is effected both by the action of a fluid and by directly-acting driven mechanical means, e.g. stirring means ; Producing cellular concrete
- B28C5/381—Producing cellular concrete
- B28C5/383—Producing cellular concrete comprising stirrers to effect the mixing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01F—MIXING, e.g. DISSOLVING, EMULSIFYING OR DISPERSING
- B01F23/00—Mixing according to the phases to be mixed, e.g. dispersing or emulsifying
- B01F23/30—Mixing gases with solids
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01F—MIXING, e.g. DISSOLVING, EMULSIFYING OR DISPERSING
- B01F27/00—Mixers with rotary stirring devices in fixed receptacles; Kneaders
- B01F27/27—Mixers with stator-rotor systems, e.g. with intermeshing teeth or cylinders or having orifices
Definitions
- the invention relates to a method for producing porous gypsum paste according to the Preamble of claim 1 and a suitable mixer according to the Preamble of claim 4.
- Porous gypsum paste also called gypsum paste
- gypsum paste is used, for example, to produce Plasterboard, especially plasterboard, is used.
- the gypsum paste is produced in a plaster mixer in which Gypsum powder (hemihydrate) is mixed with water.
- Gypsum powder hemihydrate
- the gypsum paste produced in this way becomes on a continuously moving endless belt between two cardboard webs distributed. After the gypsum has set to dihydrate, it becomes cardboard and gypsum formed sheet cut into sheets and dried. To achieve a standard density of a set and dried gypsum board becomes a correspondingly high excess of water. The drying of the excess water causes high costs.
- foam is generated in a separate device and added to the gypsum slurry for pore formation in the plaster mixer.
- Another problem with this The procedure is that the foam in the plaster mixer is partially broken or large pores are formed.
- pores become Gypsum added by the anhydride and / or hemihydrate, the delayed gas generated, manufactured.
- a generic method and a generic device (mixer) for the production of porous plastering mortar, especially plaster, are from the FR 2 089 457 A known.
- the device has one with a water supply line provided mixer and a device for producing fine, in substantially stable gas bubbles in an even distribution in the turned on Mass (from plastering mortar).
- This is the facility with pressurized gas inlets the mixer, in which glass frits are held by means of a spring washer. They push the gas into the mortar slurry that has already been prepared.
- the Glass frits are arranged outside the housing walls of the mixer and connected to the mixing chamber through openings in the housing walls.
- From US 1 769 309 A is a drum for cement production with one behind Opening arranged, perforated plate known. Through the perforated plate Compressed air supplied.
- the perforation openings have a diameter of 0.79 mm (1/32 inch) or less and are 25.4 mm (1 inch) or more apart.
- FR 1 231 620 A there is a conical mixing container with a stirring element and with Air supply on the floor between two rubber washers, the upper of which perforated is described.
- EP 0 438 772 A discloses a batch mixer for mixing and pelletizing or granulating with a container with a wall segment porous gas permeable material through which the bed of mix is fluidized.
- the object of the invention is to develop a method for producing porous gypsum paste according to the preamble of claim 1 and a corresponding mixer according to the preamble of claim 4 so that the entry of the gas bubbles formed in the paste is evened out.
- the invention is intended to enable pastes with the lowest possible water content, which are suitable for the production of boards or similar building materials with a dry bulk density of less than 1000 kg / m 3 .
- a method for producing a porous gypsum paste is first in a mixing room of a mixer binder and mixing water mixed to a gypsum paste of certain homogeneity, then in the same or in a further mixing room of the mixer, the gypsum paste, if necessary with further mixing, moving past the walls surrounding the mixing room and the gypsum paste through these walls via at least one porous element Supply element supplied a gas under excess pressure compared to the mixing room.
- the supply of the gas for pore formation requires a certain homogeneity of the Mixture of solid and water. Therefore, the gas of the mixture first supplied once a gypsum paste is made with a certain homogeneity has been.
- the gas of the gypsum paste is at least one part of these walls in the form of a porous wall section, porous Element fed.
- the pore size of the fine porous wall section should be for known plaster pastes used in the building materials industry 3 to 100 microns and the Overpressure 0.05 to 6 bar.
- the supply of gas through fine porous wall sections, which are part of the Walls are formed around the mixing room, used for pore formation in the Gypsum paste additionally the shear effect of those surrounding the wall sections Walls where the gypsum paste is moved past while mixing.
- On this Walls become gas bubbles formed in the gypsum paste in front of the wall sections separated, whereby a uniform distribution of the gas bubbles and thus a homogeneous pore formation is supported.
- One of the walls of the mixing room if necessary also a ceiling or a floor of the mixing room, as far as the gypsum paste at Mixing is moved along the ceiling or floor.
- foam and thus a porous gypsum paste, is produced by supplying the gas under pressure in the gypsum paste. Densities of less than 1000 kg / m 3 can be achieved for the building materials to be made from the gypsum paste. This saves a separate foam production.
- Foaming agents may be added to the mixing water. Foaming agents are known, for example, from the publication "Aqueous Foams", Spectrum of Science, July 1986, pages 126, 127, 132 to 138. In most cases, a much smaller amount of foaming agent is required than with a separate foam production.
- Good pore formation i.e. H. the formation of evenly distributed gas bubbles medium size, was at pore sizes according to claim 2 of 10 to 30 microns fine porous wall section and an overpressure of at least 0.1 bar found.
- H. the formation of evenly distributed gas bubbles medium size
- the invention has particularly great economic importance
- Gypsum pastes with this water / gypsum ratio can be processed with the inventive method to building materials with a density of less than 600 kg / m 3 .
- the conventional processes separate foam generation was irreplaceable.
- To achieve a porous gypsum paste significantly fewer foaming agents, namely 10 to 500 ppm, for. B. about 100 g of surfactant per 1000 kg of hemihydrate required.
- An inventive mixer according to claim 4 is for performing a Suitable method according to claim 1. It is equipped with feed facilities of gypsum and mixing water, with a mixing room for mixing gypsum and Mixing water to a gypsum paste, with walls of this or another Mixing room, where a supply element for gas supply with at least one porous element and is arranged with at least one pressure chamber and optionally with mixing elements in the mixing room or rooms.
- the porous element is a fine-porous wall section of a part of the walls surrounding the mixing room, whose pore size is 3 to 100 ⁇ m is ..
- a mixer according to claim 5 is particularly good for carrying out a Suitable method according to claim 2.
- the fine porous wall section can according to Claim 6 have a sintered metal with a thickness of 2 to 10 mm. Sintered metals are also compared to changing fine porous materials thin wall thicknesses of 2 to 10 mm are sufficiently stable to hold the gas under pressure to supply the gypsum paste. Thin wall thicknesses have the advantage of being thin Construction volume.
- a trough mixer has a trough-shaped trough forming a mixing space Side walls 1, a bottom 2 and end walls 3, the side walls 1 and the bottom 2 are formed by a U-shaped sheet.
- the trough is at his End walls 3 rotatably arranged on connection piece 5 via bearing 4.
- the bearings 4 are located in the lower third of the end walls 3.
- On one longitudinal edge of the trough is one Pour lip 6 provided.
- the trough mixer also has mixing elements, namely one or two pivotable into the mixing room inside the trough Stirrer 7 on.
- the stirrers 7 are each arranged near an end wall 3. In Figure 1 shows only a stirrer.
- a feed element is on the ropes opposite the pouring lip 6 on the Side wall 1 in the lower area of the trough and in the area of the stirrer 7 arranged, with several fine porous wall sections 8 of the feed element as Part of the side wall 1 are formed.
- the feed element of the trough mixer is included an outer wall 9 and end walls 10 provided.
- the outer wall 9 has one horizontally arranged section of a half pipe, which with the end walls 10 is welded on.
- the outer wall 9 is pressure-tight on the side wall 1 welded. It has a connection 11 for compressed air on an end wall 10.
- the side wall 1 has openings into which pressure-tight, the fine-porous wall sections 8 made of a sintered metal with a thickness of 6 mm and a pore size of 30 ⁇ m are used.
- the fine-porous wall sections 8 made of a sintered metal with a thickness of 6 mm and a pore size of 30 ⁇ m are used.
- the outer wall 9, the end wall 10 and the side wall 1 with the fine porous wall sections 8 in the area of the outer wall 9 form a Pressure chamber 12.
- the dimensions of a trough are: length 2 m, height 0.7 m and width 0.7 m.
- hemihydrate and mixing water with a water / gypsum ratio of 0.6 to 0.8 mixed with each other by first mixing the water into the Trough mixer passed, then fed the hemihydrate and both through Stirrer 7 is mixed with each other to gypsum paste.
- the gypsum porridge is made by the fine porous wall sections 8 of the supply element a gas, namely air, under slightly overpressure compared to the pressure in the mixing room.
- a mass of 385 kg of mixing water containing 50 g of surfactant is mixed with 550 kg of hemihydrate.
- the water / gypsum ratio is 0.7.
- dried gypsum boards with a density of about 600 kg / m 3 are produced in a conventional process. Without the addition of gas, gypsum boards with a density of 1100 kg / m 3 would be obtained.
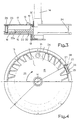
- a disc mixer according to the invention for. B. a plaster mixer, consists in essentially of a flat cylindrical housing, in which one on one Bearing 13 mounted rotor disk 15 rotatable by a vertical shaft 14 is arranged.
- the rotor disk 15 has a coarse toothing 16 at its edge on. At least one is located in a housing cover 17 of the housing Water inlet 18 and an inlet 19 for solids at a slightly greater distance from Wave than the water inlet (s) 18.
- the Rotor disk 15 has a thickening in the vicinity of the shaft 14, which is below the water inlets 18 merges into an outer ring zone.
- Housing base 20 is at least one outlet 21 near the edge and at least one meterable water supply line 22 within the toothing 16 of the Rotor disk 15 limited area arranged.
- Between the water supply line 22 and the area delimited by the toothing 15 of the rotor disk 14 is in the small space between the housing base 19 and rotor disc 15 a annular, labyrinthine constriction 22 a.
- At least one fine-porous wall section 23 of the feed element is part of one Housing shell 24 executed and within a third of the scope, which in Direction of rotation 25 on the outlet 21 or on the rear in the direction of rotation 25 Spout 21 follows, arranged.
- the fine porous stretches Wall section 23 within a small area of the third, namely in one Angular range of about 55 to 80 degrees starting from the rear spout 21.
- the Housing jacket 24 is in the region of the fine porous wall section 23 by a outer jacket section 26 and radial end walls 27 as a double jacket executed. The end walls 27 and the jacket section 26 are against each other and on Housing jacket 24 attached pressure-tight and form with the fine porous Wall section 23 a pressure chamber 29.
- the jacket section 26 has one Connection 28 for compressed air.
- the fine porous wall section 23 also exists made of a sintered metal with a thickness of 6 mm and a pore size of 30 ⁇ m. In FIG. 3 is also one between the shaft 14 and the housing cover 17 arranged seal 30 to see.
- the diameter of the disc mixer is, for example, 650 mm.
- the housing jacket 24 as a double jacket with an inner jacket made of sintered metal and an outer jacket Housing jacket built up.
- the sintered metal corresponds to the sintered metal Wall sections 23.
- the inner jacket made of sintered metal is partial, in particular in the area of the outlets 21, covered. Point to pick up the inner jacket the housing base 20 and the housing cover 17 grooves.
- the housing cover 17 can consist of two parts. This alternative allows the usual Assembling the disc mixer.
- mixing water and gypsum hemihydrate are added to the rotor disk 15, which is driven at a speed of about 300 revolutions per minute.
- a mixture of the mixing water with the hemihydrate powder already takes place on the rotor disk 15 during transport to the outside. This mixture is mixed further in the region of the toothing 16 of the rotor disk 15.
- a small part of the mixing water, z. B. 7% supplied through the water connection 22 from below, flows to the outside, is evenly distributed over the circumference through the labyrinthine constriction 22 a and then mixed with the gypsum paste.
- a disk mixer according to the invention of Example 3 corresponds to that of Example 1 except for the arrangement of a further explained below Supply element.
- Disc mixer an annular not to be seen in Figure 5, at the edge of the Housing bottom 20 arranged and attached to it and a disk additional plate 32 fastened to the rotor disk 15.
- the plate 32 has emergency running properties; d. H. the rotor disc 15 can the over a bearing surface Rotate plate 32 on the housing base 20.
- the plate 32 is, for example made of teflon.
- the fine-porous bottom portion 31 forms part of the annular disk and is like the arranged in the housing shell 24 porous wall portion 23 of the Example 2 in a smaller range for example from 55 to 80 ° within the Third of the circumference that follows the rear outlet 21 in the direction of rotation 25, arranged.
- the disc and the porous bottom portion 31 abut the Housing jacket 24, with a seal 33 arranged on the outer edge the porous bottom portion 31 and the disc pressure-tight with the Housing bottom 20 connects.
- At the radial edges of the bottom section 31 are the bottom portion 31 and the disc corresponding to each other beveled that the edges of the disc lie on the bottom portion 31.
- the bottom portion 31 is also bevelled on the inner circumference and over a Seal 34 pressure-tightly connected to the housing base 20.
- the seal 34 can extend over the entire inner edge of the bottom portion 31 and Extend the disc.
- the housing base 20 has a itself over the bottom portion 31 except for its beveled edges and its A pressure chamber 35 extending over the edge 34 of the seal forming recess 36 in the housing base 20.
- the recess 36 has the shape of a segment section.
- the housing base has inside the recess 36 20 a bore 37 and a connection 38 for compressed air.
- the radial extent of the disk and the fine-porous base section 31 extends from the housing jacket 24 to under the toothing 16 of the Rotor disk 15. Between the disk or the fine-porous base section 31 and the rotor disk 15 and the tooth flanks of the toothing 16 is located only a small space of a size in the range of about 1 mm. Also is between the plate 32 and the housing base 20 except for one middle, annular area with a recess 39 in the housing base 20 only a small space in the range of about 1 mm. Below the recess 39, the housing base 20 has a bore 40 with another Compressed air connection 41.
- An alternative to this disc mixer has additional, identical structures fine porous floor sections that are in an angular range of 90 to 180 degrees starting from the rear outlet 21 in the direction of rotation 25 arranged one behind the other are on.
- the operation of the disc mixer of example 3 corresponds to that of example 2, the compressed air instead of through the housing jacket 24 through the housing base 20 and the fine porous bottom portion 31 is supplied.
- Compressed air through the bore 40, the recess 39 in the space fed between the housing base 20 and plate 32. This is for avoidance of deposits of set gypsum paste under the plate 32 and the Formation of an air cushion.
- the housing jacket 20 can additionally have porous wall sections 23, in this case both through porous bottom portions 31 and porous wall section 23 compressed air can be supplied.
- a positive flow mixer of example 4 has a housing, for example four cylindrical housing sections 42 arranged horizontally one behind the other on.
- the housing sections 42 are on plug connections 23 with flanges and Dowel pins not shown by two, also not shown, over the Entire length of the housing extending tie rods connected together.
- the housing sections 42 form four chambers 44, 45, 46 and 47, through which a drivable shaft 48 protruding from the housing on one side.
- the housing has arranged one behind the other a water connection 49 and a connection 50 for Gypsum powder on.
- the shaft is connected to the Example four stirrer 51 provided.
- a screw 52 Directly after the Stirrer 51 is on the shaft 48, a screw 52, the body of which about Fills half of the chamber 44 and the screw flight up to the vicinity of Housing is enough.
- a rotor 54 In the chamber 45 arranged behind in the conveying direction 53 there is a rotor 54 on the shaft 48 and a stator 55 on the inside of the housing.
- the rotor 54 has a body of the same diameter as that of the screw 52 as well as closely arranged spiral mixing elements on the Body on.
- the stator 55 points accordingly into the spaces between the Mixing elements of the rotor 54 projecting mixing elements.
- the fine porous wall section 58 can as in this example, almost over the entire length of the housing section 42 extend, d. H. it is designed as a cylindrical wall section 58.
- the fine porous wall section 58 is of a second cylindrical Surround housing section 59, so that between the fine porous wall section 58 and the surrounding housing section 59, a pressure chamber 60 is formed.
- a connection 61 for compressed air In the back room 47 there is a scraper plate 62 and an outlet 63.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Structural Engineering (AREA)
- Preparation Of Clay, And Manufacture Of Mixtures Containing Clay Or Cement (AREA)
- Compounds Of Alkaline-Earth Elements, Aluminum Or Rare-Earth Metals (AREA)
- Mixers Of The Rotary Stirring Type (AREA)
- Medicinal Preparation (AREA)
Description
Claims (9)
- Verfahren zur Herstellung einer porigen Gipspaste, wobei zunächst in einem Mischraum eines Mischers Gips und Anmachwasser zu einer Gipspaste gewisser Homogenität gemischt werden, anschließend die Paste, ggfs. unter weiterem Mischen, in demselben oder in einem weiteren Mischraum an den Mischraum umgebenden Wänden vorbeibewegt wird und der Gipspaste durch diese Wände über mindestens ein poröses Element (8, 23, 31, 58) eines Zufuhrelementes ein Gas unter Überdruck im Vergleich zum Mischraum zugeführt wird, dadurch gekennzeichnet, dass der Gipspaste das Gas durch mindestens ein als Teil dieser Wände in Form eines feinporösen Wandabschnittes (8, 23, 31, 58) mit einer Porenweite von 3 bis 100 µm ausgebildetes, poröses Element unter einem Überdruck von 0,05 bis 6 bar zugeführt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass die Porenweite des feinporösen Wandabschnittes (8, 23, 31, 58) 10 bis 30 µm beträgt.
- Verfahren nach einem der Ansprüche 1 oder 2, dadurch gekennzeichnet, dass die Gipspaste durch Mischen von Halbhydrat und Anmachwasser mit einem Wasser/Gipsverhältnis von 0,6 bis 0,8 hergestellt wird.
- Mischer zur Herstellung einer porigen Gipspaste mit Einrichtungen zur Zufuhr von Gips und Anmachwasser, mit einem Mischraum zum Mischen von Gips und Anmachwasser zu einer Gipspaste, mit Wänden dieses oder eines weiteren Mischraumes, an denen ein Zufuhrelement zur Gaszufuhr zur Gipspaste mit mindestens einem porösen Element und mit (8, 23, 31, 58) mindestens einer Druckkammer angeordnet ist, und ggfs. mit Mischelementen in dem oder den Mischräumen,dadurch gekennzeichnet, dass das poröse Element als feinporöser Wandabschnitt (8, 23, 31, 58) einen Teil der den Mischraum umgebenden Wände bildet, wobei die Porenweite des feinporösen Wandabschnittes (8, 23, 31, 58) 3 bis 100 µm beträgt und Gas durch diesen Abschnitt unter einem Überdruck von 0,05 bis 6 bar zugeführt wird.
- Mischer nach Anspruch 4, dadurch gekennzeichnet, daß die Porenweite des feinporösen Wandabschnittes (8, 23, 31, 58) 10 bis 30 µm beträgt.
- Mischer nach einem der Ansprüche 4 oder 5, dadurch gekennzeichnet, daß der feinporöse Wandabschnitt (8, 23, 31, 58) ein Sintermetall einer Dicke von 2 bis 10 mm aufweist.
- Mischer nach einem der Ansprüche 4 bis 6 mit einem Trog dessen Mischraum, von Seitenwänden (1), einem Boden (2) und Stirnwänden (3) begrenzt ist und mit in den Mischraum ragenden Mischelementen (7), dadurch gekennzeichnet, dass mindestens ein feinporöser Wandabschnitt (8) des Zufuhrelementes einen Teil der Seitenwände (1) oder der Stirnwand (3) des Troges bilden und in der Nähe der Mischelemente (7) angeordnet ist.
- Mischer nach einem der Ansprüche 4 bis 6 mit einem zylindrischen Gehäuse mit einer um die senkrechte Gehäuseachse (14) drehbaren Rotorscheibe (15), die an ihrem Rand eine grobe Verzahnung (16) aufweist, im Gehäuse mit mindestens einem Wassereinlauf (18) und mindestens einem Einlass (19) für feste Stoffe im Gehäusedecker (17) und mit mindestens einem Auslauf (21) im Gehäuseboden (20) unterhalb der Verzahnung (16) der Rotorscheibe (15), dadurch gekennzeichnet, dass mindestens ein feinporöser Wandabschnitt (23, 31) des Zufuhrelementes einen Teil eines Gehäusemantels (24) oder einen radial äußeren Teil des Gehäusebodens (20) bildet und im ersten Drittel des Umfangs in Drehrichtung (25) auf den hinteren Auslauf (21) folgend angeordnet ist.
- Mischer nach einem der Ansprüche 4 bis 6, der als Zwangsdurchlaufmischer mit mehreren hintereinander angeordneten Kammern (44, 45, 46, 47) ausgebildet ist, wobei in mindestens einer vorderen Kammer Mischelemente angeordnet sind, dadurch gekennzeichnet, dass mindestens ein feinporöser Wandabschnitt (58) des Zufuhrelementes als einen Teil eines Gehäuseabschnittes einer hinteren Kammer (46) ausgebildet ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19830665 | 1998-07-09 | ||
| DE19830665A DE19830665C2 (de) | 1998-07-09 | 1998-07-09 | Verfahren zur Herstellung poriger Pasten, insbesondere porigem Gipsbrei, und Mischer |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0972621A2 EP0972621A2 (de) | 2000-01-19 |
| EP0972621A3 EP0972621A3 (de) | 2001-08-16 |
| EP0972621B1 true EP0972621B1 (de) | 2003-09-03 |
Family
ID=7873441
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99110837A Expired - Lifetime EP0972621B1 (de) | 1998-07-09 | 1999-06-05 | Verfahren zur Herstellung poriger Pasten, insbesondere porigem Gipsbrei und Mischer |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP0972621B1 (de) |
| AT (1) | ATE248692T1 (de) |
| DE (2) | DE19830665C2 (de) |
| DK (1) | DK0972621T3 (de) |
| ES (1) | ES2207068T3 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP6322353B2 (ja) * | 2013-12-17 | 2018-05-09 | 吉野石膏株式会社 | 混合攪拌機、混合攪拌方法及び軽量石膏ボード製造方法 |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1769309A (en) * | 1928-06-22 | 1930-07-01 | John A Rice | Apparatus for producing cellular cementitious material |
| FR1231620A (fr) * | 1957-08-07 | 1960-09-30 | Appareil de malaxage pneumatique pour production de plâtres aérés ou expansés | |
| LU60690A1 (de) * | 1970-04-09 | 1972-03-02 | ||
| DE3506209A1 (de) * | 1985-02-22 | 1986-08-28 | Wilhelm 6833 Waghäusel Haase | Verfahren zum herstellen von moertelmischungen oder dergleichen und mischer zur durchfuehrung des verfahrens |
| DE3865603D1 (de) * | 1987-09-02 | 1991-11-21 | Babcock Bsh Ag | Mischer zum herstellen von moertel aus feinkoernigen bindemitteln, insbesondere gips. |
| DE4002099A1 (de) * | 1990-01-25 | 1991-08-01 | Draiswerke Gmbh | Mischer |
| NL9101009A (nl) * | 1991-06-11 | 1993-01-04 | Airspray Int Bv | Mengkamer voor het met elkaar mengen van een gasvormig en een vloeibaar bestanddeel. |
| WO1997022567A1 (de) * | 1995-12-20 | 1997-06-26 | Henkel Kommanditgesellschaft Auf Aktien | Zusammensetzung zur erzeugung von leichtgips, herstellung der eingesetzten treibmittel und ihre verwendung |
-
1998
- 1998-07-09 DE DE19830665A patent/DE19830665C2/de not_active Expired - Fee Related
-
1999
- 1999-06-05 ES ES99110837T patent/ES2207068T3/es not_active Expired - Lifetime
- 1999-06-05 EP EP99110837A patent/EP0972621B1/de not_active Expired - Lifetime
- 1999-06-05 DK DK99110837T patent/DK0972621T3/da active
- 1999-06-05 AT AT99110837T patent/ATE248692T1/de not_active IP Right Cessation
- 1999-06-05 DE DE59906829T patent/DE59906829D1/de not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| ES2207068T3 (es) | 2004-05-16 |
| DE59906829D1 (de) | 2003-10-09 |
| DE19830665C2 (de) | 2003-08-28 |
| ATE248692T1 (de) | 2003-09-15 |
| EP0972621A3 (de) | 2001-08-16 |
| DE19830665A1 (de) | 2000-01-20 |
| EP0972621A2 (de) | 2000-01-19 |
| DK0972621T3 (da) | 2004-01-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69428619T2 (de) | Mischer für die Vorbereitung von Gipsgegenständen | |
| DE69631414T2 (de) | Verfahren zum vorbereiten eines geschäumten gipsgegenstands | |
| DE2133320C3 (de) | Verfahren zum Herstellen eines Formkörpers mit mindestens einem durchgehenden Hohlraum aus einem mit Flüssigkeit abbindenden pulverförmigen und einem festigen Bestandteil | |
| DE2920025C2 (de) | Vorrichtung zum kontinuierlichen Herstellen und Fördern von Putzmörtel oder dergleichen | |
| DE69421505T2 (de) | Mischvorrichtung und Verfahren | |
| DE19723426C1 (de) | Verfahren zur Herstellung einer leichten, offenporigen, mineralischen Dämmplatte | |
| DE69501365T2 (de) | Vorrichtung zum kontinuierlichen Mischen von Flüssigkeit und Pulver | |
| EP0120812A2 (de) | Verfahren und Vorrichtung zur Herstellung und unmittelbaren Anwendung von gebrauchsfertigen Baustoffzubereitungen | |
| DE3103492A1 (de) | Randverstaerkte gips-leichtbauplatte | |
| DE69807268T2 (de) | Verfahren und Vorrichtung zum Mahlen von Zementklinker mittels einer vertikalen Walzenmühle | |
| WO2012042012A1 (de) | Mischeinrichtung für pumpfähige gemische und darauf bezogenes verfahren | |
| WO1982002358A1 (en) | Method and device for the production and optionally the discharge of foam-mixtures composed of binding agents and additives | |
| DE3119811C2 (de) | Verfahren zur kontinuierlichen Herstellung von spritzfähigem Naßbeton sowie Vorrichtung zur Durchführung des Verfahrens | |
| WO2018149899A1 (de) | Verfahren zur herstellung eines betonbaustoffes | |
| DE4327074A1 (de) | Verfahren zur Herstellung einer mineralischen Leicht-Dämmplatte | |
| DE69013605T2 (de) | Ein zerkleinertes Polystyrol-Aggregat enthaltende Zementzusammensetzungen. | |
| DE1951564A1 (de) | Verfahren und Vorrichtung zum fortlaufenden Mischen von Paste fuer elektrische Batterien | |
| DE3733409C2 (de) | ||
| EP0305707B1 (de) | Mischer zum Herstellen von Mörtel aus feinkörnigen Bindemitteln, insbesondere Gips | |
| DE2021881A1 (de) | Verfahren und Vorrichtung zum kontinuierlichen Mischen von koernigen Materialien | |
| DE19830665C2 (de) | Verfahren zur Herstellung poriger Pasten, insbesondere porigem Gipsbrei, und Mischer | |
| EP0705641B1 (de) | Mischvorrichtung zum Aufschäumen von pastösen Stoffen | |
| DE102011102988B4 (de) | Mischer zur Herstellung von Suspensionen und Verfahren | |
| DE102011109520A1 (de) | Verfahren und Vorrichtung zur kontinuierlichen Erzeugung von Mineralschäumen | |
| DE1947365A1 (de) | Verfahren zum Herstellen eines zellfoermigen Werkstoffes sowie fester,wasserabgebundener zellfoermiger Schaumstoff mit einem anorganischen,hydraulischen Bindemittel |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE DE DK ES FI FR GB IE IT NL SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| RIC1 | Information provided on ipc code assigned before grant |
Free format text: 7B 28C 5/38 A, 7B 28C 5/16 B, 7B 01F 3/06 B, 7B 01F 7/00 B |
|
| 17P | Request for examination filed |
Effective date: 20020218 |
|
| AKX | Designation fees paid |
Free format text: AT BE DE DK ES FI FR GB IE IT NL SE |
|
| 17Q | First examination report despatched |
Effective date: 20020516 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: GRENZEBACH BSH GMBH |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE DE DK ES FI FR GB IE IT NL SE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REF | Corresponds to: |
Ref document number: 59906829 Country of ref document: DE Date of ref document: 20031009 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20040112 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2207068 Country of ref document: ES Kind code of ref document: T3 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040604 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20100618 Year of fee payment: 12 Ref country code: FR Payment date: 20100706 Year of fee payment: 12 Ref country code: FI Payment date: 20100621 Year of fee payment: 12 Ref country code: ES Payment date: 20100628 Year of fee payment: 12 Ref country code: DK Payment date: 20100625 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20100624 Year of fee payment: 12 Ref country code: AT Payment date: 20100621 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20100622 Year of fee payment: 12 Ref country code: BE Payment date: 20100625 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20100622 Year of fee payment: 12 Ref country code: GB Payment date: 20100401 Year of fee payment: 12 Ref country code: DE Payment date: 20100325 Year of fee payment: 12 |
|
| BERE | Be: lapsed |
Owner name: *GRENZEBACH BSH G.M.B.H. Effective date: 20110630 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20120101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110605 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20110605 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110605 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110605 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 248692 Country of ref document: AT Kind code of ref document: T Effective date: 20110605 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20120229 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110630 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59906829 Country of ref document: DE Effective date: 20120103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110605 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110630 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110605 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110606 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20131029 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110606 |