EP0679122B1 - Procede de gaufrage d'une feuille a un ou plusieurs plis - Google Patents
Procede de gaufrage d'une feuille a un ou plusieurs plis Download PDFInfo
- Publication number
- EP0679122B1 EP0679122B1 EP94904672A EP94904672A EP0679122B1 EP 0679122 B1 EP0679122 B1 EP 0679122B1 EP 94904672 A EP94904672 A EP 94904672A EP 94904672 A EP94904672 A EP 94904672A EP 0679122 B1 EP0679122 B1 EP 0679122B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sheet
- cylinders
- embossing
- cylinder
- plies
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004049 embossing Methods 0.000 title claims abstract description 34
- 238000000034 method Methods 0.000 title claims abstract description 14
- 239000002184 metal Substances 0.000 claims description 10
- 239000000853 adhesive Substances 0.000 claims description 5
- 230000001070 adhesive effect Effects 0.000 claims description 5
- 239000000126 substance Substances 0.000 claims description 3
- 238000009434 installation Methods 0.000 description 10
- 238000004519 manufacturing process Methods 0.000 description 6
- 229910000831 Steel Inorganic materials 0.000 description 4
- 238000003490 calendering Methods 0.000 description 4
- 239000010959 steel Substances 0.000 description 4
- 230000002745 absorbent Effects 0.000 description 3
- 239000002250 absorbent Substances 0.000 description 3
- 239000000463 material Substances 0.000 description 3
- 238000004026 adhesive bonding Methods 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- 238000003466 welding Methods 0.000 description 2
- 238000010521 absorption reaction Methods 0.000 description 1
- 206010000496 acne Diseases 0.000 description 1
- 229920002678 cellulose Polymers 0.000 description 1
- 239000001913 cellulose Substances 0.000 description 1
- 238000010073 coating (rubber) Methods 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 230000000994 depressogenic effect Effects 0.000 description 1
- 239000013536 elastomeric material Substances 0.000 description 1
- 239000011888 foil Substances 0.000 description 1
- 239000003292 glue Substances 0.000 description 1
- 238000004513 sizing Methods 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F—MECHANICAL WORKING OR DEFORMATION OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F1/00—Mechanical deformation without removing material, e.g. in combination with laminating
- B31F1/07—Embossing, i.e. producing impressions formed by locally deep-drawing, e.g. using rolls provided with complementary profiles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F—MECHANICAL WORKING OR DEFORMATION OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F2201/00—Mechanical deformation of paper or cardboard without removing material
- B31F2201/07—Embossing
- B31F2201/0707—Embossing by tools working continuously
- B31F2201/0715—The tools being rollers
- B31F2201/0723—Characteristics of the rollers
- B31F2201/0728—Material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F—MECHANICAL WORKING OR DEFORMATION OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F2201/00—Mechanical deformation of paper or cardboard without removing material
- B31F2201/07—Embossing
- B31F2201/0707—Embossing by tools working continuously
- B31F2201/0715—The tools being rollers
- B31F2201/0741—Roller cooperating with a non-even counter roller
- B31F2201/0743—Roller cooperating with a non-even counter roller having a matching profile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F—MECHANICAL WORKING OR DEFORMATION OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F2201/00—Mechanical deformation of paper or cardboard without removing material
- B31F2201/07—Embossing
- B31F2201/0758—Characteristics of the embossed product
- B31F2201/0761—Multi-layered
- B31F2201/0764—Multi-layered the layers being nested
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F—MECHANICAL WORKING OR DEFORMATION OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F2201/00—Mechanical deformation of paper or cardboard without removing material
- B31F2201/07—Embossing
- B31F2201/0784—Auxiliary operations
- B31F2201/0787—Applying adhesive
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H21/00—Non-fibrous material added to the pulp, characterised by its function, form or properties; Paper-impregnating or coating material, characterised by its function, form or properties
- D21H21/14—Non-fibrous material added to the pulp, characterised by its function, form or properties; Paper-impregnating or coating material, characterised by its function, form or properties characterised by function or properties in or on the paper
- D21H21/40—Agents facilitating proof of genuineness or preventing fraudulent alteration, e.g. for security paper
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/10—Methods of surface bonding and/or assembly therefor
- Y10T156/1002—Methods of surface bonding and/or assembly therefor with permanent bending or reshaping or surface deformation of self sustaining lamina
- Y10T156/1007—Running or continuous length work
- Y10T156/1023—Surface deformation only [e.g., embossing]
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/17—Surface bonding means and/or assemblymeans with work feeding or handling means
- Y10T156/1702—For plural parts or plural areas of single part
- Y10T156/1712—Indefinite or running length work
- Y10T156/1737—Discontinuous, spaced area, and/or patterned pressing
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/17—Surface bonding means and/or assemblymeans with work feeding or handling means
- Y10T156/1702—For plural parts or plural areas of single part
- Y10T156/1712—Indefinite or running length work
- Y10T156/1741—Progressive continuous bonding press [e.g., roll couples]
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/24—Structurally defined web or sheet [e.g., overall dimension, etc.]
- Y10T428/24628—Nonplanar uniform thickness material
- Y10T428/24669—Aligned or parallel nonplanarities
Definitions
- the invention relates to the field of fibrous products, including sanitary and household papers, wadding cellulose. It relates to a method of embossing a sheet with one or several folds in order for use as toilet paper, towel or paper towel in particular.
- US Patent 3940529 describes an absorbent two-ply product.
- the folds each have a pattern made by embossing with depressed areas and raised areas.
- the raised areas on a fold are arranged between the raised areas of the other fold, and the connection is made by mechanical welding sides between the bottom and the top of the reliefs. This mechanical welding results in a loss of mechanical strength with perforation of the sheet at this level.
- the installation includes two metallic embossing cylinders, provided with reliefs or pimples, meshing with each other.
- the spacing between the elementary reliefs is less than their width so that the sheet is strongly compressed along the sides of these reliefs, and welded.
- Patent application EP A 499 942 describes an embossed sheet comprising protuberances on one side, the thickness of the sheet being the smallest at the level of the foot of the protuberances.
- US Patent 4,325,773 describes a method of assembling two plies where the latter have been previously embossed separately.
- the two embossing cylinders, meshing one in the other, ensure the association of the folds.
- the pattern of embossing consists of elongated reliefs relatively spaced from each other other.
- US Patent 4,759,967 describes an embossing method for a multiple sheet consisting in bonding the plies together beforehand by means of an adhesive spray then to emboss the sheet between two metallic embossing cylinders.
- the embossing pattern on the cylinders consists of alternating cavities with raised areas by relation to the plane of the surface.
- the two cylinders mesh with each other, the reliefs of a cylinder engaging in the cavities of the second. It should be noted that these cylinders have been engraved together.
- the thickness e1 at the ply bonding areas is less than that e2 of the zones, intermediate between two bonding zones, which form pockets of air.
- the subject of the invention is a method of manufacturing by embossing a sheet of at least one fold in which it is engaged between two metal cylinders provided protuberances. rotated by means known per se, and meshing one inside the other with a clearance e1 between the top of the protuberances of a cylinder and the surface of the cylinder opposite, and a clearance e2 between the sides of two adjacent protuberances.
- This process is characterized in that e1 and e2 are determined in the cross direction with respect to the machine direction in such a way that the ratio e1 / e2 is between 0.8 and 1.
- a sheet is obtained which combines the advantage a rubber / steel embossing and a steel / steel embossing that is to say a sheet whose thickness is substantially uniform, while presenting an improved softness by the effect of calendering produced on the top of the raised areas of the sheet.
- one make a sheet with at least two folds by bringing at least one of the two folds to match the surface of one of the cylinders by applying it by means of a rubber cylinder.
- the game e1 is between 5/100 and 5/10 mm and corresponds at most to the sum of the thicknesses folds constituting the sheet.
- a sheet at least two folds which, compared to a sheet of the prior art of the nested type, "nested", can include a number of larger bosses. This results in better resistance to the crash.
- diameter rollers can be obtained lower for the same sheet length, which reduces the storage volume.
- the calendering effect produced by the contact with the two metal cylinders provides softness touch.
- the number of protrusions is greater than 12 per cm 2 .
- Figure 1 shows, in cross section, a sheet 1 of the prior art with two folds 2 and 3 nested one inside the other.
- the method of manufacturing such a sheet is taught for example in US patent 3556907.
- the fold 2 has bosses 4 obtained by embossing. these bosses are regularly spaced from each other others and facing fold 3 which also has bosses 5, facing the fold 2. These are nested between the bosses 4. The spacing between bosses 4 and 5 is sufficient to create a gap 6 between them.
- the thickness of the sheet varies between a minimum value e1 to where the bosses of a fold are in contact with the fold opposite, and an e2 value between two adjacent bosses.
- the e1 / e2 ratio is low, of the order of 0.1.
- e1 corresponds the thickness of the 2 folds of absorbent crepe paper, by example 0.2 mm and e2 was measured at 1.85 mm.
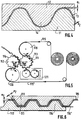
- Figure 2 shows the embossing interval of two cylinders, in section in the plane passing through the axis of the two cylinders.
- the metal cylinder 7 has radial projections 8 evenly distributed on the surface: likewise the 7 'cylinder has projections 8 'of the same dimension.
- the usual technique of engraving a pair of such cylinders consists in engraving a first cylinder by means of a wheel in one harder material than that of the cylinder. Once this first cylinder made, the second cylinder is engraved using the first so as to obtain two conjugate patterns which overlap perfectly one in the other.
- FIG. 3 An installation has been shown diagrammatically in FIG. 3 embossing 10 of a single-ply sheet or multiple sheet previously linked, with two cylinders 11, 12 arranged in parallel and driven by conventional means in the sense arrows. Cylinders 11, 12, metallic or another equivalent material, are provided, on the surface, with pins 13, 14, extending radially outward.
- the cylinders are positioned relative to each other by so as to mesh with each other, the pins 13 of the cylinder 11 coming to be placed between the pins 14 of cylinder 12 in the embossing interval.
- Sheet 15 of crepe paper is engaged between cylinders 11 and 12 and emerges by presenting on each face of the bosses corresponding to the pins of the cylinders.
- Figure 4 is an enlarged view of a section made by a plane passing through the axis of the two cylinders and represents a configuration of the pins according to the invention.
- the pins are identical on the two cylinders and are distributed in the same pattern with walking directions, respectively cross direction, identical.
- the walking direction is that of the sheet scroll direction; the creping lines him are perpendicular.
- We define the cross direction as forming a plus or minus 45 ° angle to the perpendicular to the direction market.
- the pattern has a cross direction perpendicular to the running direction.
- the pins have a height of between 0.5 and 1.5 mm.
- the embossing interval between the two cylinders is equal to e1 between the top of the pins 13 of the first cylinder and the bottom of the engraving between the two adjacent pins 14 of the second cylinder. It is equal to e2 between the sides of two adjacent pins 13 and 14.
- the pins are symmetrical by relative to their axis.
- the clearance e1 is a function of the spacing that has been set between the two cylinders.
- the value of the e2 game depends on the geometric parameters of the pins. So, for a step P of the pattern given, it is a function of the apex angle ⁇ of the pins as well as of their width L at the top. In practice the angle ⁇ is understood between 25 and 35 ° and the width at the top is 0.1 and 1.2 mm.
- e1 and e2 are determined so that the ratio e1 / e2 is less than or equal to 1 and greater than 0.8.
- the value e1 will be chosen at most equal to the thickness of the embossing sheet. This ensures calendering of the sheet at the top of the bosses obtained, providing a improved softness to the touch.
- FIG. 5 shows an embossing installation for the formation of a two-ply sheet.
- This installation in itself of the conventional type comprises two cylinders 111, 112, made of metal or in an equivalent material, arranged in parallel and driven by conventional means in the direction of the arrows.
- the cylinders 111 and 112 are provided with pins 113, 114 extending radially outwards and meshing with each other.
- a pressure cylinder 119, 120 to rubber coating, or other elastomeric material, is associated to each of the cylinders 111 and 112.
- crepe paper 115, 115 ′ Two folds of crepe paper 115, 115 ′ are engaged respectively between the cylinders 111 and 119, and 112 and 120 and are pressed on their respective embossing cylinder whose relief they espouse.
- a gluing device 121 also known per se, deposits an adhesive substance on the vertices of the raised areas of fold 115, then the two folds are entrained in the embossing interval between the two cylinders 111 and 112 where they join in a leaf.
- This sheet 115-115 ' is then transformed into a finished product such as for example household paper towel.
- FIG. 6 represents an enlarged view of a section made along a plane passing through the axis of the two cylinders 111 and 112.
- the two folds 115, 115 ' substantially follow the outline of pins 113 and 114 respectively.
- the clearance between the two cylinders is equal to e1 between the peaks of the spikes and the bottom of the engraving facing it. he is equal to e2 at the flanks.
- determine the clearance e1 so that it is at most equal to the thickness of the two folds so as to ensure on the one hand the bonding by gluing at this level, on the other hand, a calendering action.
- the geometry of the pins is determined so that the ratio e1 / e2 is between 0.8 and 1. This ensures the formation of a sheet, where the air pocket is reduced.
- FIG. 7 shows an embodiment of a 3-ply sheet. The installation is similar to that of the figure 5. Each common element has been designated by the same reference. She includes an additional sizing machine 122 and a supply of 115 '' paper.
- Each of the glueers 121, 122 deposits an adhesive substance on at least part of the tops of the reliefs of the folds 115 and 115 '. These are applied against the metal cylinders 111 and 112 by means of the rubber cylinders 119, 120.
- the two folds 115, 115 ' are driven in the direction of the arrows as far as the engagement interval of the two cylinders 111 and 112.
- a third fold 115 '' is drawn between the two folds 115, 115 'at time of their engagement in said interval.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Machines For Manufacturing Corrugated Board In Mechanical Paper-Making Processes (AREA)
- Laminated Bodies (AREA)
- Sanitary Thin Papers (AREA)
- Folding Of Thin Sheet-Like Materials, Special Discharging Devices, And Others (AREA)
- Paper (AREA)
Description
Claims (7)
- Procédé de gaufrage d'une feuille de papier crêpé à au moins un pli selon lequel on engage celle-ci entre deux cylindres métalliques pourvus de protubérances, entraínés en rotation par des moyens connus en soi, en s'engrenant l'un dans l'autre avec un jeu e1 entre le sommet des protubérances d'un cylindre et la surface en vis-à-vis de l'autre cylindre, et un jeu e2 entre les flancs de deux protubérances adjacentes, caractérisé en ce que l'on détermine e1 et e2 dans le sens travers par rapport au sens de défilement de papier de façon que le rapport e1/e2 soit compris entre 0,8 et 1.
- Procédé de gaufrage selon la revendication 1 caractérisé en ce que l'on détermine e1 et e2 dans le sens machine de défilement du papier de façon que le rapport e1/e2 soit compris entre 0,2 et 1 et de préférence entre 0,2 et 0,5.
- Procédé de gaufrage d'une feuille à au moins deux plis, selon la revendication 1 ou 2, caractérisé en ce que l'on amène au moins l'un des deux plis à se conformer préalablement à la surface de l'un desdits cylindres en l'appliquant sur celui-ci au moyen d'un cylindre à revêtement caoutchouc.
- Procédé, selon la revendication précédente, caractérisé en ce que l'on applique les deux plis séparément sur les cylindres métalliques au moyen de cylindres à revêtement caouchouc.
- Procédé, selon l'une des revendications 3 et 4, caractérisé en ce qu'on dépose une substance adhésive sur au moins une partie des zones en relief avant engagement des plis entre les deux cylindres métalliques.
- Procédé de gaufrage d'une feuille de papier crêpé selon l'une des revendications précédentes, caractérisé en ce que le jeu e1 est compris entre 5/100 et 5/10 mm et correspond au plus à la somme des épaisseurs des plis constituant la feuille.
- Procédé de gaufrage selon la revendication précédente caractérisé en ce que le nombre de protubérances est supérieur à 12 au cm2.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9300366 | 1993-01-15 | ||
| FR9300366A FR2700496B1 (fr) | 1993-01-15 | 1993-01-15 | Procédé de gaufrage d'une feuille à un ou plusieurs plis, feuille de papier gaufré. |
| PCT/FR1994/000042 WO1994015776A1 (fr) | 1993-01-15 | 1994-01-13 | Procede de gaufrage d'une feuille a un ou plusieurs plis, feuille de papier gaufre |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0679122A1 EP0679122A1 (fr) | 1995-11-02 |
| EP0679122B1 true EP0679122B1 (fr) | 1998-08-19 |
Family
ID=9443074
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP94904672A Expired - Lifetime EP0679122B1 (fr) | 1993-01-15 | 1994-01-13 | Procede de gaufrage d'une feuille a un ou plusieurs plis |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US5686168A (fr) |
| EP (1) | EP0679122B1 (fr) |
| AT (1) | ATE169862T1 (fr) |
| DE (1) | DE69412585T2 (fr) |
| ES (1) | ES2121186T3 (fr) |
| FR (1) | FR2700496B1 (fr) |
| WO (1) | WO1994015776A1 (fr) |
Families Citing this family (45)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2746702B1 (fr) * | 1996-03-27 | 1998-05-29 | James River | Procede de fabrication d'une feuille absorbante |
| DE19804736C1 (de) * | 1998-02-06 | 1999-02-25 | Windmoeller & Hoelscher | Schweißzylinder |
| WO1999044814A1 (fr) * | 1998-03-02 | 1999-09-10 | Fabio Perini S.P.A. | Procede et dispositif de production d'un materiau en bande continue gaufre et produit ainsi obtenu |
| US6059003A (en) * | 1998-07-29 | 2000-05-09 | Integrated Design Corporation | Web heating and pressing apparatus |
| US6261666B1 (en) | 1998-08-14 | 2001-07-17 | Paper Converting Machine Co. | Two-ply paper products with either nested or foot-to-foot embossments and method of making |
| US6109326A (en) * | 1998-08-20 | 2000-08-29 | Paper Converting Machine Company | Embosser for producing two-ply paper products with either nested or foot-to-foot embossments |
| US6277466B1 (en) * | 1998-11-23 | 2001-08-21 | The Procter & Gamble Company | Embossed multi ply cellulosic fibrous structure and process for producing the same |
| US6421052B1 (en) | 1999-04-09 | 2002-07-16 | The Procter & Gamble Company | Method of seaming and expanding amorphous patterns |
| US6872342B2 (en) * | 1999-04-09 | 2005-03-29 | The Procter & Gamble Company | Embossing and adhesive printing process |
| US6148496A (en) | 1999-04-09 | 2000-11-21 | The Procter & Gamble Company | Method for making a seamless apertured metal belt |
| US6193918B1 (en) | 1999-04-09 | 2001-02-27 | The Procter & Gamble Company | High speed embossing and adhesive printing process and apparatus |
| IT246987Y1 (it) | 1999-08-06 | 2002-05-02 | C M G Costruzioni Meccaniche G | Macchina trasformabile per la alvorazione superficiale di carta |
| US7118796B2 (en) * | 1999-11-01 | 2006-10-10 | Fort James Corporation | Multi-ply absorbent paper product having impressed pattern |
| CA2324786C (fr) | 1999-11-01 | 2014-02-25 | Fort James Corporation | Produit en papier absorbant multicouches a motifs imprimes |
| US6602577B1 (en) | 2000-10-03 | 2003-08-05 | The Procter & Gamble Company | Embossed cellulosic fibrous structure |
| ES2260179T3 (es) * | 2001-06-29 | 2006-11-01 | Georgia-Pacific France | Procedimiento de fabricacion de una hoja de guata de celulosa gofrada y cilindro de gofrado. |
| US6846172B2 (en) * | 2002-06-07 | 2005-01-25 | The Procter & Gamble Company | Embossing apparatus |
| US7314663B2 (en) * | 2003-09-29 | 2008-01-01 | The Procter + Gamble Company | Embossed multi-ply fibrous structure product and process for making same |
| US7967950B2 (en) * | 2003-09-29 | 2011-06-28 | The Procter & Gamble Company | High bulk strong absorbent single-ply tissue-towel paper product |
| ITFI20040032A1 (it) * | 2004-02-13 | 2004-05-13 | Perini Fabio Spa | Metodo e dispositivo goffratore e laminatore per la produzione di manufatti plurivelo e relativo prodotto |
| ITFI20040053A1 (it) * | 2004-03-04 | 2004-06-04 | Perini Fabio Spa | Prodotto plurivelo in carta o simili, metodo per la sua produzione e relativo impianto |
| ITFI20050032A1 (it) * | 2005-03-01 | 2006-09-02 | Perini Fabio Spa | Metodo e dispositvo per la giunzione di veli di carta |
| US7524404B2 (en) * | 2005-06-08 | 2009-04-28 | The Procter & Gamble Company | Embossing process including discrete and linear embossing elements |
| US7435316B2 (en) * | 2005-06-08 | 2008-10-14 | The Procter & Gamble Company | Embossing process including discrete and linear embossing elements |
| US7785696B2 (en) * | 2005-06-08 | 2010-08-31 | The Procter & Gamble Company | Embossed product including discrete and linear embossments |
| US7829177B2 (en) * | 2005-06-08 | 2010-11-09 | The Procter & Gamble Company | Web materials having offset emboss patterns disposed thereon |
| US7597777B2 (en) | 2005-09-09 | 2009-10-06 | The Procter & Gamble Company | Process for high engagement embossing on substrate having non-uniform stretch characteristics |
| US20070062658A1 (en) * | 2005-09-21 | 2007-03-22 | Wiwi Kevin M | Absorbent paper product having high definition embossments |
| ITFI20060245A1 (it) | 2006-10-11 | 2008-04-12 | Delicarta Spa | Un materiale in carta con elevate caratteristiche detergenti e metodo per la sua produzione |
| ITFI20070048A1 (it) * | 2007-02-27 | 2008-08-28 | Perini Fabio Spa | Gruppo goffratore multi-funzione |
| US20100030174A1 (en) * | 2008-08-04 | 2010-02-04 | Buschur Patrick J | Multi-ply fibrous structures and processes for making same |
| US20100028621A1 (en) * | 2008-08-04 | 2010-02-04 | Thomas Timothy Byrne | Embossed fibrous structures and methods for making same |
| US20100297378A1 (en) * | 2009-05-19 | 2010-11-25 | Andre Mellin | Patterned fibrous structures and methods for making same |
| US8753737B2 (en) * | 2009-05-19 | 2014-06-17 | The Procter & Gamble Company | Multi-ply fibrous structures and methods for making same |
| US8282775B2 (en) | 2009-05-19 | 2012-10-09 | The Procter & Gamble Company | Web substrate having optimized emboss area |
| US20100297395A1 (en) * | 2009-05-19 | 2010-11-25 | Andre Mellin | Fibrous structures comprising design elements and methods for making same |
| US8328984B2 (en) | 2009-05-19 | 2012-12-11 | The Procter & Gamble Company | Web substrate having optimized emboss design |
| US9243368B2 (en) * | 2009-05-19 | 2016-01-26 | The Procter & Gamble Company | Embossed fibrous structures and methods for making same |
| ITFI20110135A1 (it) * | 2011-07-07 | 2013-01-08 | Futura Spa | Dispositivo e metodo per la produzione di materiale caratceo nastriforme. |
| US20140004307A1 (en) | 2012-06-29 | 2014-01-02 | The Procter & Gamble Company | Textured Fibrous Webs, Apparatus And Methods For Forming Textured Fibrous Webs |
| EP2685000B1 (fr) * | 2012-07-10 | 2015-09-09 | Sca Tissue France | Étoffe non-tissé à texture proche de celle du tissu comprenant des fibres papetières, rouleau de calandrage et son procédé de fabrication |
| NL2010296C2 (en) * | 2013-02-13 | 2014-08-14 | Unga B V | Stackable cards. |
| US10060062B2 (en) | 2013-02-22 | 2018-08-28 | The Procter & Gamble Company | Equipment and processes for the application of atomized fluid to a web substrate |
| US8858213B2 (en) | 2013-02-22 | 2014-10-14 | The Procter & Gamble Company | Equipment and processes for the application of atomized fluid to a web substrate |
| ES2578830B1 (es) * | 2015-01-29 | 2017-08-10 | L.C. Paper 1881, S. A. | Procedimiento de obtención de papel gofrado de capa única y unidad de gofrado de una lámina de papel crepado de capa única |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1245280A (en) * | 1967-11-09 | 1971-09-08 | Kimberly Clark Co | Two-sided cellulose towel and method of making |
| US3708366A (en) * | 1970-11-25 | 1973-01-02 | Kimberly Clark Co | Method of producing absorbent paper toweling material |
| IT1063742B (it) * | 1976-01-29 | 1985-02-11 | F I L C A S S A S Di Cristofor | Perfezionamento ai procedimenti ai dispositivi per la produzione di carte goffrate per la formazione di cuscinetti stratificati e cuscinetti cartacei prodotti secondo il per fezionamento |
| DE2611325C3 (de) * | 1976-03-17 | 1978-09-07 | Bhs-Bayerische Berg-, Huetten- Und Salzwerke Ag, 8000 Muenchen | Einseitige Wellpappenmaschine |
| US4325768A (en) * | 1979-03-19 | 1982-04-20 | American Can Company | Method of manufacturing fibrous sheet structure |
| DE3804611A1 (de) * | 1988-02-13 | 1989-08-24 | Casaretto Robert Kg | Walzenanordnung zum verfestigen von vlies od.dgl. |
| CA2060567C (fr) * | 1991-02-04 | 1997-06-10 | Galyn Arlyn Schulz | Machine pour gaufrer une bande fibreuse |
| CA2052746A1 (fr) * | 1991-02-22 | 1992-08-23 | Jerome Steven Veith | Methode de gaufrage de bandes |
| US5294475A (en) * | 1992-06-12 | 1994-03-15 | The Procter & Gamble Company | Dual ply cellulosic fibrous structure laminate |
-
1993
- 1993-01-15 FR FR9300366A patent/FR2700496B1/fr not_active Expired - Fee Related
-
1994
- 1994-01-13 ES ES94904672T patent/ES2121186T3/es not_active Expired - Lifetime
- 1994-01-13 AT AT94904672T patent/ATE169862T1/de not_active IP Right Cessation
- 1994-01-13 DE DE69412585T patent/DE69412585T2/de not_active Expired - Fee Related
- 1994-01-13 WO PCT/FR1994/000042 patent/WO1994015776A1/fr not_active Ceased
- 1994-01-13 EP EP94904672A patent/EP0679122B1/fr not_active Expired - Lifetime
- 1994-01-13 US US08/491,895 patent/US5686168A/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| DE69412585T2 (de) | 1999-01-07 |
| ATE169862T1 (de) | 1998-09-15 |
| FR2700496B1 (fr) | 1995-02-17 |
| FR2700496A1 (fr) | 1994-07-22 |
| US5686168A (en) | 1997-11-11 |
| EP0679122A1 (fr) | 1995-11-02 |
| DE69412585D1 (de) | 1998-09-24 |
| WO1994015776A1 (fr) | 1994-07-21 |
| ES2121186T3 (es) | 1998-11-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0679122A1 (fr) | Procede de gaufrage d'une feuille a un ou plusieurs plis | |
| EP0765215B1 (fr) | Feuille multicouche de papier absorbant, son procede de fabrication | |
| EP1209289B1 (fr) | Feuille de papier absorbant crêpé, cylindre pour le gaufrage et procédé de fabrication d'une telle feuille | |
| EP1047546B1 (fr) | Feuille de papier absorbant gaufre, son procede de fabrication et dispositif permettant de la fabriquer | |
| CA2458952C (fr) | Produit en papier absorbant presentant un gaufrage ameliore | |
| EP0793751B1 (fr) | Feuille multicouche absorbante et son procede de fabrication | |
| EP0876537B1 (fr) | Feuille stratifiee a gaufrage mixte | |
| EP1101866B2 (fr) | Feuille de papier absorbant crêpé et gaufré, cylindre de gaufrage et procédé de gaufrage | |
| EP1670991B1 (fr) | Feuille de papier absorbant | |
| EP2170596B1 (fr) | Feuille de papier absorbant crêpé, cylindre de gaufrage d'une telle feuille et procédé de gaufrage | |
| FR2728152A1 (fr) | Papier absorbant gaufre a motifs combines | |
| EP0572503A1 (fr) | Feuilles de papier multicouches presentant des marquages, procede et dispositif pour leur elaboration. | |
| EP0570579B1 (fr) | Feuilles complexes de papier absorbant | |
| EP1081284B1 (fr) | Produit en papier absorbant comprenant au moins trois plis et son procédé de fabrication | |
| EP1159487B1 (fr) | Produit en papier absorbant comprenant deux ou trois plis | |
| EP0828602B1 (fr) | Procede de fabrication d'une structure absorbante | |
| CA2202166C (fr) | Papier absorbant gaufre a motifs combines | |
| CA2223015C (fr) | Procede de fabrication d'une structure absorbante |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19950816 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FR GB GR IE IT LI NL PT SE |
|
| 17Q | First examination report despatched |
Effective date: 19951124 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: JAMES RIVER |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: FORT JAMES FRANCE |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FR GB GR IE IT LI NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980819 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19980819 |
|
| REF | Corresponds to: |
Ref document number: 169862 Country of ref document: AT Date of ref document: 19980915 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 69412585 Country of ref document: DE Date of ref document: 19980924 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19981005 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2121186 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: FRENCH |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19981119 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19981119 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 19980819 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990131 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990131 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20031224 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PT Payment date: 20031231 Year of fee payment: 11 Ref country code: GB Payment date: 20031231 Year of fee payment: 11 Ref country code: BE Payment date: 20031231 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20040105 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20040121 Year of fee payment: 11 Ref country code: DE Payment date: 20040121 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20040128 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050113 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050113 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050113 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050114 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050713 |
|
| BERE | Be: lapsed |
Owner name: *FORT JAMES FRANCE Effective date: 20050131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050802 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20050113 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050930 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MM4A Effective date: 20050713 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20050801 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20050114 |
|
| BERE | Be: lapsed |
Owner name: *FORT JAMES FRANCE Effective date: 20050131 |