EP0624431B1 - Outillage pour l'application de toile abrasive sur une machine d'usinage par toilage de portées cylindriques sur des pièces - Google Patents
Outillage pour l'application de toile abrasive sur une machine d'usinage par toilage de portées cylindriques sur des pièces Download PDFInfo
- Publication number
- EP0624431B1 EP0624431B1 EP94400578A EP94400578A EP0624431B1 EP 0624431 B1 EP0624431 B1 EP 0624431B1 EP 94400578 A EP94400578 A EP 94400578A EP 94400578 A EP94400578 A EP 94400578A EP 0624431 B1 EP0624431 B1 EP 0624431B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- arm
- lining
- axis
- tooling
- journal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 230000010355 oscillation Effects 0.000 claims description 3
- 239000000463 material Substances 0.000 claims description 2
- 229920003051 synthetic elastomer Polymers 0.000 claims description 2
- 239000005061 synthetic rubber Substances 0.000 claims description 2
- 238000003754 machining Methods 0.000 description 16
- 239000004744 fabric Substances 0.000 description 9
- 235000019589 hardness Nutrition 0.000 description 8
- 230000003370 grooming effect Effects 0.000 description 5
- 230000007547 defect Effects 0.000 description 3
- 230000006978 adaptation Effects 0.000 description 2
- 230000001360 synchronised effect Effects 0.000 description 2
- 230000008878 coupling Effects 0.000 description 1
- 238000010168 coupling process Methods 0.000 description 1
- 238000005859 coupling reaction Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 229920001971 elastomer Polymers 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000005060 rubber Substances 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B5/00—Machines or devices designed for grinding surfaces of revolution on work, including those which also grind adjacent plane surfaces; Accessories therefor
- B24B5/36—Single-purpose machines or devices
- B24B5/42—Single-purpose machines or devices for grinding crankshafts or crankpins
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B21/00—Machines or devices using grinding or polishing belts; Accessories therefor
- B24B21/004—Machines or devices using grinding or polishing belts; Accessories therefor using abrasive rolled strips
Definitions
- the present invention relates to a tool for the application of abrasive cloth on a machine for grooming spans cylindrical on parts, in particular trunnions and crank pins on crankshafts.
- Machines of this type known for example by the request for EP-A-0 366 506 of the applicant include, for each mounted on a workpiece, a pivoting arm that can be moved vertically carrying three abrasive cloth application pads arranged substantially at the three angles of an equilateral triangle. A first of these three pads is mounted in a high middle position on the arm and two others in low lateral position on two articulated jaws on the arm and coupled so that they can be tightened together the other by synchronous pivoting in opposition, under the action of a common maneuver.
- the arm is movable vertically under the action of a balancing cylinder with controlled supply pressure.
- the three pads apply a abrasive cloth with uniform pressure against the surface to be machined.
- the cloth application pads abrasive have a circular arc application surface spanning a relatively small angle, usually less than 30 °. These tools work well for the state of surface areas.
- the present invention relates to a tool for applying canvas abrasive allowing a machining by canvas of greater precision on the cylindrical bearings of parts, in particular the trunnions and the crankshaft crankpins.
- the abrasive cloth application tool which is the subject of the present invention is intended for a machine for the machining by grinding of cylindrical bearings on parts, in particular journals and crankshaft pins, machine of the type comprising, for each bearing to machining, a pivoting and vertically movable arm carrying three pads for applying abrasive cloth disposed substantially at the three angles of an equilateral triangle.
- each of said pads has a concave application surface in an arc extending over an angle greater than 60 ° and less than 120 ° so that the three pads virtually completely enclose the surface to be machined.
- the three pads apply the abrasive cloth against the surface to be machined, not only each with the same pressure, but also with a practically uniform pressure over their whole angular length. This ensures optimal compensation for any shape defects (ovalization, runout, etc.) of the litter.
- this pad is mounted with a limited mobility in horizontal translation perpendicular to the axis of the span to be machined.
- each lateral shoe is mounted on its jaw by a parallel axis to the axis of the bearing surface to be machined, with limited mobility oscillation around its axis.
- each skate comprises a rigid base bearing a more flexible filling, with a low coefficient of fiction.
- This lining can for example be made of a rubber vulcanized synthetic on the base.
- the lining can advantageously have along its axis of curvature increasing in hardness from the middle to the two ends of the width of the trim.
- the lining can include five sections, namely a low middle section hardness followed towards each end of an intermediate section of medium hardness itself followed by a large end section hardness.
- these three hardnesses can correspond to 90, 95 and 98 Shore.
- the grooming tool in accordance with the invention is used on a machine according to the patent application EP-A-0366 506 for the abrasive machining of cylindrical surfaces on parts, in particular for the machining by trunnion of the pins and crankshaft crankpins.
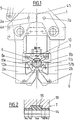
- Figure 1 we recognize an arm 1 freely mounted pivoting about a horizontal axis on a slide not shown vertically movable. Arm 1 has two jaws 2a and 2b articulated by horizontal axes 3a and 3b on the arm 1 and coupled by toothed segments 4a, 4b so that they can be pressed against each other by synchronous pivoting in opposition by relative to the arm 1, under the action of a common actuating cylinder 5.
- a first shoe 7 is mounted in the middle position on the arm 1 and two other pads 8a and 8b are mounted in a lateral position on the two jaws 2a and 2b in such a way that when the three pads 7, 8a and 8b are tightened, under the action of the jack 5, against the cylindrical bearing 6 to be machined, for application against this surface 6 of a fabric abrasive 9, the three pads 7, 8a and 8b are arranged substantially at the three angles of an equilateral triangle and, due to the balancing of the mass of arm 1 by a balancing means not shown, by example a cylinder with controlled supply pressure, the three pads are applied with uniform pressure against the scope 6 to to machine.
- each shoe 7, 8a, 8b extends over an angle slightly less than 120 °, so that the three pads practically completely cover the surface 6 to be machined.
- the median shoe 7 upper is mounted on arm 1 with limited mobility in horizontal translation perpendicular to the axis of the staff 6.
- both pads 8a, 8b lower side are mounted on the jaws 2a and 2b by horizontal axes 12a and 12b parallel to the axis of the bearing surface 6 to be machined, with mobility limited in oscillation around their axes.
- the mobility of the three pads 7, 8a and 8b ensures optimal adaptation of the pads on the surface of the surface 6 to be machined, regardless of tolerances of the structure of the arm 1 and in particular of the clearances which may occur at the toothed segments 4a, 4b coupling the two jaws 2a and 2b.
- the upper shoe 7 comprises a rigid base 13, in this case metallic, the concave inner surface in an arc carries a gasket 14 in a more flexible material, with a low coefficient of friction, for example a vulcanized synthetic rubber.
- Dovetail profiling 15 improves the connection of the lining 14 with the base 13.
- the machining by linen of the cylindrical seat 6 involves not only a rotational movement of the staff 6, but also, in a manner known per se, an oscillating movement of the bearing 6 along its axis (with a view to obtaining a drawing cross machining), and that the width of each shoe 7, 8 is less at the width of the bearing surface 6 to be machined, the two end parts of the width of the span 6 only undergo alternating machining while the middle part is subjected to permanent machining, which can lead to inaccuracies in range.
- the lining 14 can advantageously understand, along its axis of curvature, several sections of hardness different, increasing from the middle of the width towards both ends.
- the tool according to the invention could be used also on machines other than those corresponding to the patent application EP-A-0366 506, although the latter, due to their structure, lead to particularly machining results favorable.
- the pads have an angular length greater than 60 and less than 120 °, preferably between about 90 and 110 °.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Grinding Of Cylindrical And Plane Surfaces (AREA)
- Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)
- Polishing Bodies And Polishing Tools (AREA)
Description
Grâce à leur forme enveloppante sur légèrement moins de 120° et à leur montage particulier sur le bras, les trois patins appliquent la toile abrasive contre la portée à usiner non seulement chacun avec la même pression, mais encore avec une pression pratiquement uniforme sur toute leur longueur angulaire. Cela assure une compensation optimale des éventuels défauts de forme (ovalisation, faux-rond, etc) de la portée.
Claims (5)
- Outillage pour l'application de toile abrasive sur une machine d'usinage par toilage de portées cylindriques sur des pièces, notamment des tourillons et manetons sur des vilebrequins, comprenant, pour chaque portée (6) à usiner, un bras (1) pivotant et mobile verticalement, et trois patins (7, 8) d'application de toile abrasive montés, un premier (7) en position médiane haute sur le bras (1) et les deux autres (8) en position latérale basse sur deux mâchoires (2a, 2b) articulées sur le bras et couplées de manière à pouvoir être serrées l'une contre l'autre, de telle manière que lors du serrage contre la portée (6) à usiner, les trois patins soient disposés sensiblement aux trois angles d'un triangle équilatéral, caractérisé par le fait que chacun des trois patins (7, 8) présente une surface concave d'application de toile abrasive s'étendant sur un angle supérieur à 60° et inférieur à 120° de manière que lors du sertage, les trois patins de chaque bras enveloppent pratiquement complètement la portée (6) à usiner, que le patin supérieur médian (7) est monté sur le bras (1) avec une mobilité limitée en translation horizontale perpendiculairement à l'axe de la portée (6), et que chacun des deux patins latéraux inférieurs (8a, 8b) est monté sur sa mâchoire (2a, 2b) par un axe (12a, 12b) parallèle à l'axe de la portée (6), avec une mobilité limitée en oscillation autour de son axe (12a, 12b).
- Outillage suivant la revendication 1, caractérisé par le fait que chaque patin (7, 8) comprend une embase rigide (13) et une garniture (14) en matière plus souple, à faible coefficient de friction.
- Outillage suivant la revendication 2, caractérisé par le fait que la garniture (14) est constituée par du caoutchouc synthétique vulcanisé.
- Outillage suivant la revendication 2 ou 3, caractérisé par le fait que la garniture (14) comprend, suivant l'axe de courbure, plusieurs sections (14a, 14b, 14c) de duretés différentes allant en augmentant depuis le milieu de la largeur vers les deux extrémités.
- Outillage suivant la revendication 4, caractérisé par le fait que la garniture (14) comprend une section médiane (14a) de faible dureté suivie vers chaque extrémité de deux sections intermédiaires (14b) de dureté moyenne elles-mêmes suivies de deux sections d'extrémité (14c) de dureté élevée.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9303156 | 1993-03-18 | ||
| FR9303156A FR2702693B1 (fr) | 1993-03-18 | 1993-03-18 | Outillage pour l'application de toile abrasive sur une machine d'usinage par toilage de portées cylindriques sur des pièces. |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0624431A1 EP0624431A1 (fr) | 1994-11-17 |
| EP0624431B1 true EP0624431B1 (fr) | 1998-05-27 |
Family
ID=9445126
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP94400578A Expired - Lifetime EP0624431B1 (fr) | 1993-03-18 | 1994-03-17 | Outillage pour l'application de toile abrasive sur une machine d'usinage par toilage de portées cylindriques sur des pièces |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US5522762A (fr) |
| EP (1) | EP0624431B1 (fr) |
| JP (1) | JPH0752005A (fr) |
| DE (1) | DE69410527T2 (fr) |
| ES (1) | ES2116549T3 (fr) |
| FR (1) | FR2702693B1 (fr) |
Families Citing this family (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19602974A1 (de) * | 1996-01-27 | 1997-07-31 | Thielenhaus Ernst Kg | Maschine für die Feinschleifbearbeitung einer zylindrischen Lagerfläche an einer Welle mit Hilfe eines Schleifbandes |
| FR2758756B1 (fr) * | 1997-01-30 | 1999-02-26 | Procede Machines Speciales Spm | Ensemble d'usinage par bande abrasive d'une portee cylindrique d'une piece |
| DE19850216A1 (de) * | 1998-10-31 | 2000-05-04 | Nagel Masch Werkzeug | Verfahren und Vorrichtung zur Feinbearbeitung von im wesentlichen zylindrischen Werkstückoberflächen |
| FR2808463B1 (fr) * | 2000-05-04 | 2002-09-13 | Procedes Et Machines Speciales | Machine d'usinage par bande abrasive de portees cylindriques sur des pieces |
| EP1447171B1 (fr) | 2003-02-12 | 2006-07-12 | Nissan Motor Co., Ltd. | Appareil et procédé de finition des surfaces |
| FR2872726B1 (fr) * | 2004-07-08 | 2007-11-23 | Societes Des Procedes Et Machi | Dispositif de superfinition et procede associe |
| US7169028B1 (en) * | 2005-11-02 | 2007-01-30 | Barton Ii Kenneth A | Flexible finishing shoe |
| EP2399706B9 (fr) * | 2010-06-22 | 2013-10-02 | Supfina Grieshaber GmbH & Co. KG | Dispositif de finissage pour le finissage de surfaces de pièces usinées |
| EP2650081B1 (fr) * | 2012-04-13 | 2013-11-27 | Supfina Grieshaber GmbH & Co. KG | Procédé et dispositif de finition d'une surface de pièce usinée |
| JP6037510B2 (ja) * | 2013-04-09 | 2016-12-07 | 尚一 島田 | 加工装置 |
| CN111496637B (zh) * | 2019-01-30 | 2022-04-05 | 辽宁五一八内燃机配件有限公司 | 一种可降低曲轴轴颈圆角粗糙度值的装置及方法 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4682444A (en) * | 1984-05-07 | 1987-07-28 | Industrial Metal Products Corporation | Microfinishing apparatus and method |
| DE8602817U1 (de) * | 1986-02-04 | 1986-04-10 | Maschinenbau Grieshaber GmbH & Co, 77709 Wolfach | Vorrichtung für die Bearbeitung von Lagerzapfen von Kurbelwellen od. dgl. |
| DE3813484A1 (de) * | 1988-04-21 | 1989-11-02 | Ford Werke Ag | Vorrichtung zur feinbearbeitung der hubzapfen von kurbelwellen |
| FR2636877B1 (fr) * | 1988-09-27 | 1994-07-01 | Procedes Machines Speciales | Machine pour l'usinage par abrasif de portees cylindriques sur des pieces, notamment pour l'usinage par toilage des tourillons et manetons sur des vilebrequins |
| US4993191A (en) * | 1989-04-28 | 1991-02-19 | Industrial Metal Products Corporation | Roller cam microfinishing tooling |
-
1993
- 1993-03-18 FR FR9303156A patent/FR2702693B1/fr not_active Expired - Fee Related
-
1994
- 1994-03-17 EP EP94400578A patent/EP0624431B1/fr not_active Expired - Lifetime
- 1994-03-17 DE DE69410527T patent/DE69410527T2/de not_active Expired - Fee Related
- 1994-03-17 ES ES94400578T patent/ES2116549T3/es not_active Expired - Lifetime
- 1994-03-18 US US08/210,506 patent/US5522762A/en not_active Expired - Fee Related
- 1994-03-18 JP JP6049086A patent/JPH0752005A/ja active Pending
Also Published As
| Publication number | Publication date |
|---|---|
| DE69410527T2 (de) | 1998-09-17 |
| JPH0752005A (ja) | 1995-02-28 |
| ES2116549T3 (es) | 1998-07-16 |
| FR2702693B1 (fr) | 1995-05-24 |
| FR2702693A1 (fr) | 1994-09-23 |
| EP0624431A1 (fr) | 1994-11-17 |
| US5522762A (en) | 1996-06-04 |
| DE69410527D1 (de) | 1998-07-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0680806B1 (fr) | Outillage pour le toilage de portées cylindriques avec contrÔle de diamètre des portées | |
| CA2128564C (fr) | Dispositif de nettoyage d'un cylindre | |
| EP0624431A1 (fr) | Outillage pour l'application de toile abrasive sur une machine d'usinage par toilage de portées cylindriques sur des pièces | |
| EP0501183B1 (fr) | Dispositif pour le reprofilage des rails d'une voie ferrée | |
| EP1160054B1 (fr) | Machine d'usinage par bande abrasive de portées cylindriques sur des pièces | |
| FR2644370A1 (fr) | Machine pour la mise en etat et/ou l'entretien des sols pourvue d'un outil rotatif | |
| EP0853964B1 (fr) | Patin à roulettes en ligne muni d'un frein agissant sur les roulettes | |
| FR2610857A1 (fr) | Dispositif antivibration et dispositif de guidage pour scie a ruban | |
| FR2614819A1 (fr) | Dispositif pour usiner des semelles de ski notamment pour affuter la couche de glissement et les carres d'acier | |
| FR2650529A1 (fr) | Dispositif applicateur pour machine de nappage au moyen de ruban de matiere composite | |
| EP0856379B1 (fr) | Ensemble d'usinage par bande abrasive d'une portée cylindrique d'une pièce | |
| EP0082748B1 (fr) | Machine de rectification plane frontale notamment pour rectifier les extrémités de fibres optiques | |
| EP0073725A1 (fr) | Machine pour la mise en état et/ou l'entretien des sols | |
| FR2476502A1 (fr) | Broyeur, en particulier moulin pour canne a sucre | |
| EP2014411A1 (fr) | Machine d'affûtage | |
| LU83011A1 (fr) | Dispositif de polissage en continu d'un cylindre de pression d'une bobineuse de coils | |
| FR2494298A1 (fr) | Machine pour le refendage de peaux avec lame a ruban a tranchant en position fixe pour n'importe quelle epaisseur de coupe | |
| FR2472424A1 (fr) | Dispositif et procede pour polir en continu et pour refroidir uniformement la table d'un cylindre de laminoir | |
| EP0002145B1 (fr) | Machine à poncer à bande étroite | |
| FR2694715A1 (fr) | Procédé et appareil de rectification des manetons de villebrequin. | |
| FR2805129A1 (fr) | Dispositif de guidage pour la decoupe de carcasses d'animaux de boucheries, installation pour la decoupe de carcasses comprenant un tel dispositif, et procede de decoupe de carcasses | |
| EP0108009A1 (fr) | Machine automatique à ébavurer des pièces de petites dimensions | |
| FR2841575A3 (fr) | Machine a meuler | |
| FR2791292A1 (fr) | Ensemble d'usinage de pieces par abrasif, notamment de superfinition | |
| FR2636612A1 (fr) | Machine de travail a cylindres |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES GB IT SE |
|
| 17P | Request for examination filed |
Effective date: 19950516 |
|
| 17Q | First examination report despatched |
Effective date: 19970414 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| ITF | It: translation for a ep patent filed | ||
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES GB IT SE |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19980528 |
|
| REF | Corresponds to: |
Ref document number: 69410527 Country of ref document: DE Date of ref document: 19980702 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2116549 Country of ref document: ES Kind code of ref document: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19980827 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20070316 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20080911 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20080912 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20080924 Year of fee payment: 15 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20080318 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080318 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20090317 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090317 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090317 |