CN211783249U - Quick measuring and checking tool for verticality of workpiece - Google Patents
Quick measuring and checking tool for verticality of workpiece Download PDFInfo
- Publication number
- CN211783249U CN211783249U CN201922483970.2U CN201922483970U CN211783249U CN 211783249 U CN211783249 U CN 211783249U CN 201922483970 U CN201922483970 U CN 201922483970U CN 211783249 U CN211783249 U CN 211783249U
- Authority
- CN
- China
- Prior art keywords
- workpiece
- detection
- sliding
- tool
- plate
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000001514 detection method Methods 0.000 claims abstract description 56
- 238000007689 inspection Methods 0.000 claims abstract description 23
- 230000006835 compression Effects 0.000 claims description 10
- 238000007906 compression Methods 0.000 claims description 10
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 claims description 6
- 238000003825 pressing Methods 0.000 claims description 4
- 229910052742 iron Inorganic materials 0.000 claims description 3
- 210000004907 gland Anatomy 0.000 claims 2
- 238000005259 measurement Methods 0.000 abstract description 4
- 238000003754 machining Methods 0.000 description 3
- 238000000034 method Methods 0.000 description 3
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000007812 deficiency Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000001179 sorption measurement Methods 0.000 description 1
Images


Landscapes
- A Measuring Device Byusing Mechanical Method (AREA)
Abstract
本实用新型公开了一种工件垂直度快速测量检具,其特征在于:包括检座,该检座上设有定位板、两检测表及能够于检座上滑动的滑板,所述滑板上设有定位基面一,所述定位板上设有定位基面二,所述定位板上设有两检测孔,且所述检测表的表头穿过对应检测孔与工件的检测面二接触,所述工件设置于滑板上,且工件的检测面一与定位基面一接触定位,所述工件的检测面二与定位基面二接触定位。
The utility model discloses an inspection tool for rapid measurement of the verticality of a workpiece, which is characterized by comprising an inspection seat, on which a positioning plate, two inspection tables and a sliding plate capable of sliding on the inspection seat are arranged, and the sliding plate is provided with There is a positioning base surface 1, a positioning base surface 2 is provided on the positioning plate, two detection holes are provided on the positioning plate, and the head of the detection table passes through the corresponding detection holes and contacts the detection surface 2 of the workpiece, The workpiece is arranged on the sliding plate, and the first detection surface of the workpiece is positioned in contact with the positioning base surface, and the detection surface of the workpiece is positioned in contact with the positioning base surface II.
Description
技术领域technical field
本实用新型涉及一种检具,特别是一种工件垂直度快速测量检具。The utility model relates to a checking tool, in particular to a checking tool for quickly measuring the verticality of a workpiece.
背景技术Background technique
工件在加工过程中需要进行检测以便直到加工的精度符不符合要求,为了提高效率,很多工件的检测都是在加工现场进行,但是某些简单的尺寸(如长度、宽度等)可以采用常规的检具直接检测,一些复杂的尺寸需要在三维投影测试系统中进行检测,这样检测过程复杂,而且耽误时间。The workpiece needs to be inspected during the machining process so that the machining accuracy does not meet the requirements. In order to improve efficiency, the inspection of many workpieces is carried out on the machining site, but some simple dimensions (such as length, width, etc.) can use conventional The inspection tool is directly inspected, and some complex dimensions need to be inspected in the three-dimensional projection test system, so the inspection process is complicated and time-consuming.
发明内容SUMMARY OF THE INVENTION
为了克服现有技术的不足,本实用新型提供一种工件垂直度快速测量检具。In order to overcome the deficiencies of the prior art, the utility model provides a quick measuring tool for measuring the verticality of a workpiece.
本实用新型解决其技术问题所采用的技术方案是:The technical scheme adopted by the utility model to solve its technical problems is:
工件垂直度快速测量检具,其特征在于:包括检座,该检座上设有定位板、两检测表及能够于检座上滑动的滑板,所述滑板上设有定位基面一,所述定位板上设有定位基面二,所述定位板上设有两检测孔,且所述检测表的表头穿过对应检测孔与工件的检测面二接触,所述工件设置于滑板上,且工件的检测面一与定位基面一接触定位,所述工件的检测面二与定位基面二接触定位。The inspection tool for rapid measurement of workpiece verticality is characterized in that it includes an inspection seat, and the inspection seat is provided with a positioning plate, two inspection tables and a sliding plate that can slide on the inspection seat, and the sliding plate is provided with a
所述检座上设有滑台,所述滑板位于滑台上,且滑板与滑台间设有滑动导向结构。The inspection seat is provided with a sliding table, the sliding plate is located on the sliding table, and a sliding guide structure is arranged between the sliding plate and the sliding table.
所述滑动导向结构为设置于滑台上的燕尾槽与设置于滑板上的燕尾块。The sliding guide structure is a dovetail groove arranged on the sliding table and a dovetail block arranged on the sliding plate.
所述检座上设有调节支撑板及调节手柄,调节支撑板上设有调节滑孔;所述调节手柄上设有与滑孔配合的滑轴,所述滑板上设有连接螺孔,所述调节手柄上设有沉孔,连接螺钉穿过沉孔与连接螺孔配合从而将调节手柄与滑板连接为一体,且连接螺钉上套有压紧弹簧,该压紧弹簧的一端与滑板接触且压紧弹簧的另一端与调节支撑板接触。The inspection seat is provided with an adjustment support plate and an adjustment handle, and the adjustment support plate is provided with an adjustment sliding hole; the adjustment handle is provided with a sliding shaft matched with the sliding hole, and the sliding plate is provided with a connecting screw hole, so The adjusting handle is provided with a countersink, and the connecting screw passes through the countersunk hole and cooperates with the connecting screw hole to connect the adjusting handle and the slide plate as a whole, and a compression spring is sleeved on the connection screw, and one end of the compression spring is in contact with the slide plate and is The other end of the compression spring is in contact with the adjustment support plate.
所述两检测表均通过支撑块固定于检座上。The two test tables are both fixed on the test seat through a support block.
所述滑板上设有能够压住工件的压盖,所述压盖上设有磁铁,所述滑板上设有与磁铁相吸的铁柱。The slide plate is provided with a press cover capable of pressing the workpiece, the press cover is provided with a magnet, and the slide plate is provided with an iron column that attracts the magnet.
所述两表头的中心轴线的连线与定位基面一空间垂直。The line connecting the central axes of the two meter heads is spaced perpendicular to the positioning base surface.
所述定位板上凹槽,所述凹槽内设有两凸台,一凸台位于凹槽的顶端,且另一凸台位于凹槽的底端,所述检测孔设置于相应的凸台上,且所述定位基面二为凸台的顶面。There is a groove on the positioning plate, and two bosses are arranged in the groove, one boss is located at the top end of the groove, and the other boss is located at the bottom end of the groove, and the detection holes are arranged on the corresponding bosses and the second positioning base surface is the top surface of the boss.
所述定位板上凹槽,所述凹槽内设有两凸台,一凸台位于凹槽的顶端,且另一凸台位于凹槽的底端,所述检测孔设置于相应的凸台上,且所述定位基面二为凸台的顶面。There is a groove on the positioning plate, and two bosses are arranged in the groove, one boss is located at the top end of the groove, and the other boss is located at the bottom end of the groove, and the detection holes are arranged on the corresponding bosses and the second positioning base surface is the top surface of the boss.
本实用新型的有益效果是:本实用新型两个检测表检测与检测面二上下两端点的距离,然后通过两个距离值得到一个差值,通过差值能够体现出检测面二与检测面一的垂直度的大小,该工具结构简单、容易操作,在车间就能直接使用,因而节省了时间、提高了生产效率。The beneficial effects of the utility model are: the two detection tables of the utility model detect the distance between the upper and lower ends of the
附图说明Description of drawings
下面结合附图和实施例对本实用新型进一步说明。The present utility model will be further described below in conjunction with the accompanying drawings and embodiments.
图1是本实用新型的检测视图;Fig. 1 is the detection view of the present utility model;
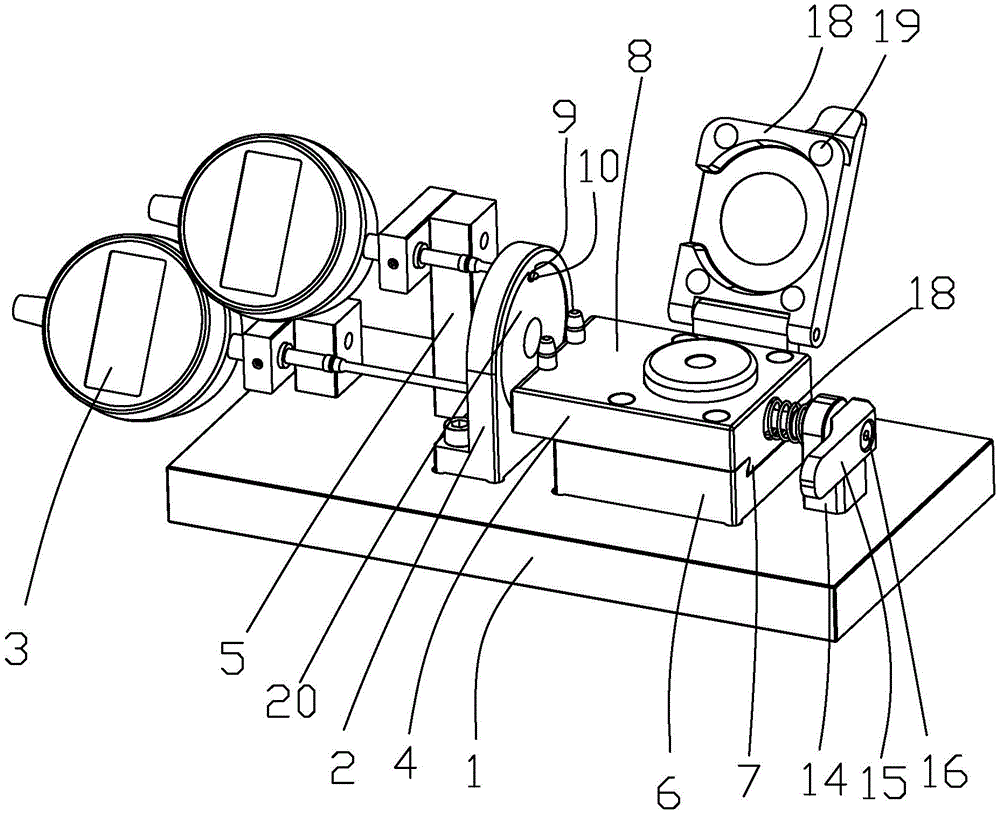
图2是本实用新型的结构视图;Fig. 2 is the structural view of the present utility model;
图3是工件的结构视图。FIG. 3 is a structural view of the workpiece.
具体实施方式Detailed ways
参照图1至图3,本实用新型公开了一种工件垂直度快速测量检具,包括方形板构成的检座1,该检座1上设有定位板2、两检测表3及能够于检座1上滑动的滑板4,所述两检测表3均通过支撑块5固定于检座1上,检测表3为百分表,滑板4具体安装结构在于:所述检座1上设有滑台6,所述滑板4位于滑台6上,且滑板4与滑台6间设有滑动导向结构,所述滑动导向结构为设置于滑台6上的燕尾槽与设置于滑板4上的燕尾块7。Referring to FIGS. 1 to 3 , the present utility model discloses an inspection tool for rapid measurement of the verticality of a workpiece, which includes an
所述滑板4上设有定位基面一8,所述定位板2上设有定位基面二9,所述定位板2上设有两与定位基面二9垂直的检测孔,且所述检测表3的表头10穿过对应检测孔与工件11的检测面二12接触,所述工件11设置于滑板4上,且工件11的检测面一13与定位基面一8接触定位,所述工件11的检测面二12与定位基面二9接触定位,上述结构中,工件11的结构为:一个圆环通过方板与圆板连接,我们需要测圆环侧面与圆板底面的垂直度,因而圆环侧面为检测面一13;而圆板底面为检测面二12。其检测原理为:因为我们可以在加工时将定位基面一8与定位基面二9的垂直度保证很好,因而当工件11的检测面一13与定位基面一8贴合后,如果检测面二12是与检测面一13完美垂直的,那么检测面二12会与定位基面二9也完美贴合,但是如果检测面二12与检测面一13不垂直,那么检测面二12在定位基面二9上会发生倾斜,因为工件11本身一般不会弯曲,因而倾斜的角度大小决定了工件11的垂直度的大小,不管怎么倾斜检测面二12总会在上或下有一个点与定位基面二9接触,因而我们在上下两点各设置了一个检测孔,所述两检测孔的中心轴线的连线与定位基面一8空间垂直,这样保证检测精确,表头10穿过对应检测孔与工件11的检测面二12接触而测得检测面二12上下两个点与定位基面二9的距离,那么我们只需通过计算上下两个点值的差值就能够知道倾斜的角度大或是小,从而也就知道检测面二12与检测面一13的垂直度的大与小,差值越大垂直度越大,差值越小垂直度越小。The
如图所示,所述检座1上设有调节支撑板14及调节手柄15,调节支撑板14上设有调节滑孔;所述调节手柄15上设有与滑孔配合的滑轴,所述滑板4上设有连接螺孔,所述调节手柄15上设有沉孔,连接螺钉16穿过沉孔与连接螺孔配合从而将调节手柄15与滑板4连接为一体,且连接螺钉16上套有压紧弹簧17,该压紧弹簧17的一端与滑板4接触且压紧弹簧17的另一端与调节支撑板14接触,上述结构是为了保证便于安装工件11以及保证检测面二12与定位基面二9的良好接触,当通过调节手柄15拉开滑板4时可以安装工件11,然后松开调节手柄15,滑板4通过压紧弹簧17使检测面二12与定位基面二9保证良好接触。As shown in the figure, the
所述滑板4上设有能够压住工件11的压盖18,所述压盖18上设有磁铁19,所述滑板4上设有与磁铁19相吸的铁柱,采用磁铁19是因为磁铁19的吸附力不会很大,避免压得工件11变形。The
如图所示,所述定位板2上凹槽20,所述凹槽20内设有两凸台,一凸台位于凹槽20的顶端,且另一凸台位于凹槽20的底端,所述检测孔设置于相应的凸台上,且所述定位基面二9为凸台的顶面,这样设置保证了检测面二12与定位基面二9的接触只能是顶端或是底端,而另一个测量点只能是底端或顶端,这样测出的数据精度高。As shown in the figure, there is a
以上对本实用新型实施例所提供的一种工件11垂直度快速测量检具,进行了详细介绍,本文中应用了具体个例对本实用新型的原理及实施方式进行了阐述,以上实施例的说明只是用于帮助理解本实用新型的方法及其核心思想;同时,对于本领域的一般技术人员,依据本实用新型的思想,在具体实施方式及应用范围上均会有改变之处,综上所述,本说明书内容不应理解为对本实用新型的限制。The above is a detailed introduction to a quick measuring tool for measuring the verticality of the
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922483970.2U CN211783249U (en) | 2019-12-30 | 2019-12-30 | Quick measuring and checking tool for verticality of workpiece |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922483970.2U CN211783249U (en) | 2019-12-30 | 2019-12-30 | Quick measuring and checking tool for verticality of workpiece |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN211783249U true CN211783249U (en) | 2020-10-27 |
Family
ID=72890904
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201922483970.2U Expired - Fee Related CN211783249U (en) | 2019-12-30 | 2019-12-30 | Quick measuring and checking tool for verticality of workpiece |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN211783249U (en) |
-
2019
- 2019-12-30 CN CN201922483970.2U patent/CN211783249U/en not_active Expired - Fee Related
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN204064194U (en) | A kind of clamp for detect aperture distance | |
| CN108088354B (en) | A measuring tool for detecting the spatial angle of elbows | |
| CN211121016U (en) | Axial dimension qualification degree testing fixture for crankshaft | |
| CN102183192A (en) | Device and method for detecting symmetry of key groove | |
| CN105423845A (en) | Guide blade back locking plate slot measuring device | |
| CN202903112U (en) | Testing fixture for detecting included angle between main shaft plane and eccentric plane of shaft parts | |
| CN111811363A (en) | A measuring device for measuring the size of V-shaped grooves | |
| CN102128579B (en) | Detecting device for measuring appearance with compound angle length | |
| CN205957845U (en) | Spindle is synthesized and is examined utensil | |
| CN205156806U (en) | Measurable quantity transverse tooth thick ness examines utensil | |
| CN108489353A (en) | A Combined Multifunctional Measuring Device | |
| CN108645326B (en) | Gauge for measuring symmetry degree of journal excircle pin hole relative to axial lead | |
| CN203605885U (en) | Crankcase comprehensive test tool | |
| CN206223061U (en) | A kind of counterbore depth dimensions detection means | |
| CN215296076U (en) | height gauge | |
| CN203824467U (en) | Outer arc intersection point position and bounce measuring tester | |
| CN202304801U (en) | Differential meter seat of crankshaft phase angle checking jig | |
| CN210533227U (en) | Static precision measuring device for guide rail pair | |
| CN115704663A (en) | Device and method for detecting test piece machining accuracy | |
| CN205957844U (en) | Bridge plate for measuring position precision between prismatic guide rail and dovetail guide rail | |
| CN219589604U (en) | Measuring tool structure for measuring profile of blade edge plate surface of aero-engine | |
| CN224004357U (en) | Bearing groove center diameter measuring device | |
| CN205619864U (en) | Long and narrow work piece straightness accuracy measuring apparatu structure | |
| CN206514760U (en) | Error checking arrangement is advised in twisting machine drum shaft positioning of weaving | |
| CN223425913U (en) | A compressor vane verticality inspection tool |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20201027 |