CN211734510U - Workpiece fixing device for electroplating outside cylinder body tank - Google Patents
Workpiece fixing device for electroplating outside cylinder body tank Download PDFInfo
- Publication number
- CN211734510U CN211734510U CN201922177969.7U CN201922177969U CN211734510U CN 211734510 U CN211734510 U CN 211734510U CN 201922177969 U CN201922177969 U CN 201922177969U CN 211734510 U CN211734510 U CN 211734510U
- Authority
- CN
- China
- Prior art keywords
- workpiece
- pressing
- pressing rod
- longitudinal beam
- bottom plate
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Electroplating Methods And Accessories (AREA)
Abstract
本实用新型公开了一种用于缸体槽外电镀的工件固定装置,包括固定架和压紧组件;固定架包括底板和固定于底板的框架;压紧组件用于将工件压紧在底板上并锁定;本实用新型配合辅助安装机构,可在本实用新型上安装辅助安装组件,使得工件固定安装于本实用新型后被移送至电镀的各个工位,形成模块式固定,方便更换,配合以安装辅助机构,可适用于不同的工件,且不需更换阳极,因而也不需停止生产线,适合于各种尺寸的的工件,实现产品的“无缝切换”,避免停线的产能损失,迅速满足交付需求,将成熟产品的切换时间减至最小,将产能损失降到最低。
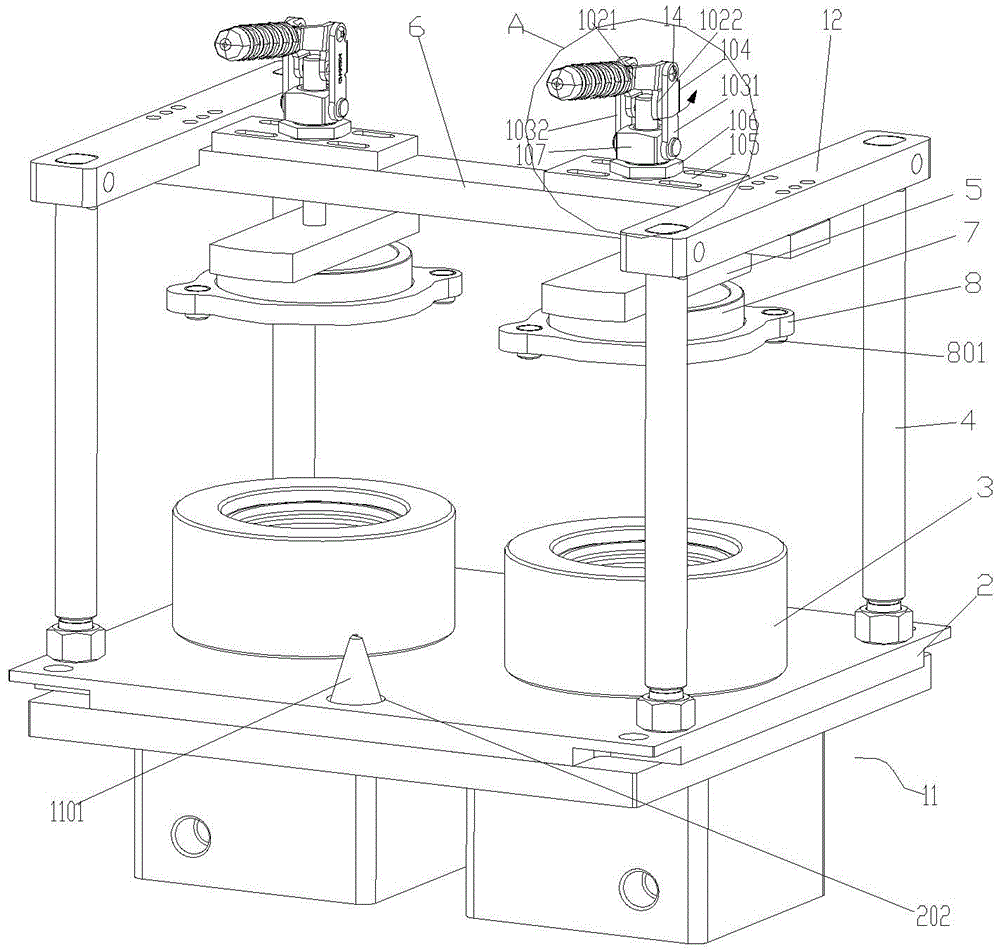
The utility model discloses a workpiece fixing device for electroplating outside a tank of a cylinder body, which comprises a fixing frame and a pressing component; the fixing frame comprises a bottom plate and a frame fixed on the bottom plate; the pressing component is used for pressing the workpiece on the bottom plate The utility model cooperates with the auxiliary installation mechanism, and the auxiliary installation components can be installed on the utility model, so that the workpiece is fixedly installed in the utility model and then transferred to each station of electroplating, forming a modular fixation, which is convenient for replacement. The installation auxiliary mechanism can be applied to different workpieces, and it does not need to replace the anode, so there is no need to stop the production line. It is suitable for workpieces of various sizes, realizes "seamless switching" of products, avoids the loss of production capacity when the line is stopped, and quickly Meet delivery demands, minimize switchover time for mature products, and minimize capacity loss.
Description
技术领域technical field
本实用新型涉及一种缸体电镀装置部件,特别涉及用于缸体槽外电镀的工件固定装置。The utility model relates to a part of a cylinder body electroplating device, in particular to a workpiece fixing device used for electroplating outside a cylinder body groove.
背景技术Background technique
缸体作为发动机、柱塞泵、往复式压缩机等设备的主要部件,用于与活塞、缸头共同组成工作空间;以发动机为例则组成燃烧室,并为活塞组件提供运动轨迹,从而形成动力转换环境。气缸在引导活塞不断进行往复运动的过程中,气缸内壁与活塞之间长时间、高频率地互相摩擦,导致气缸作用的有用功率降低,消耗一部分能量。为解决上述问题,采用在内壁进行电镀,以电镀镀层来代替缸套解决上述问题。现有技术中,槽外循环电镀由于形成流动电镀环境,保证了镀层上的阳离子实时更替,无差别的浓度和稳定均匀的流动性,保证了镀层的密实紧致,保证电镀质量。As the main component of the engine, plunger pump, reciprocating compressor and other equipment, the cylinder block is used to form the working space together with the piston and the cylinder head; taking the engine as an example, it forms the combustion chamber and provides the movement trajectory for the piston assembly, thus forming a Power conversion environment. In the process of guiding the piston to reciprocate continuously, the inner wall of the cylinder and the piston rub against each other for a long time and at a high frequency, which reduces the useful power of the cylinder and consumes a part of the energy. In order to solve the above problems, the inner wall is electroplated, and the electroplating layer is used instead of the cylinder liner to solve the above problems. In the prior art, the circulating electroplating outside the tank ensures real-time replacement of cations on the coating layer, undifferentiated concentration and stable and uniform fluidity due to the formation of a flowing electroplating environment, ensuring the compactness of the coating layer and the quality of electroplating.
但现有的槽外电镀结构中,由于缸体(工件)的外形尺寸各不相同,需要更换阳极(特别是高度)才能用于电镀工作的正常进行,需要整个生产线停工,提高损耗,提高生产成本;而且工装夹具也各不相同,结构复杂,更换过程需人工进行,降低工作效率。However, in the existing electroplating structure outside the tank, due to the different external dimensions of the cylinder (workpiece), the anode (especially the height) needs to be replaced to be used for the normal electroplating work, and the entire production line needs to be shut down to increase the loss and increase the production Moreover, the fixtures are also different, the structure is complex, and the replacement process needs to be carried out manually, which reduces the work efficiency.
因此,需要对现有的循环电镀的工装进行改进,具有通用性,适合于各种尺寸的工件,实现产品的“无缝切换”,避免停线的产能损失,迅速满足交付需求,将成熟产品的切换时间减至最小,将产能损失降到最低。Therefore, it is necessary to improve the existing cyclic electroplating tooling, which is versatile, suitable for workpieces of various sizes, realizes "seamless switching" of products, avoids the loss of production capacity due to stoppage, quickly meets the delivery demand, and converts mature products. Changeover times are minimized and capacity losses are minimized.
实用新型内容Utility model content
有鉴于此,本实用新型的目的是提供一种发动机缸体槽外电镀的通用型工装,具有通用性,适合于各种尺寸的工件,实现产品的“无缝切换”,避免停线的产能损失,迅速满足交付需求,将成熟产品的切换时间减至最小,将产能损失降到最低。In view of this, the purpose of the present utility model is to provide a universal tooling for electroplating outside the engine block groove, which has versatility, is suitable for workpieces of various sizes, realizes "seamless switching" of products, and avoids the production capacity of line shutdown. Loss, quickly meet delivery needs, minimize switchover time for mature products, and minimize capacity loss.
本实用新型的用于缸体槽外电镀的工件固定装置,包括安装架组件,所述安装架组件包括固定架和压紧组件;The workpiece fixing device for electroplating outside the cylinder groove of the utility model comprises an installation frame assembly, and the installation frame assembly includes a fixing frame and a pressing assembly;
所述固定架包括底板和固定于底板的框架;The fixing frame includes a base plate and a frame fixed on the base plate;
所述压紧组件用于将工件压紧在底板上并锁定;The pressing assembly is used for pressing and locking the workpiece on the base plate;
本实用新型使用时,配合安装辅助组件使用,在补偿了高度和直径等尺寸后,工件安装于工装后被移送至电镀的各个工位,通过与工件配套的安装辅助组件调整总体高度与阳极形成配合,不同的工件不需更换阳极,因而也不需停止生产线,更换不同的工件直接安装于本工装且安放于电镀装置即可,配套的安装辅助组件还能在工件与电镀装置之间形成过渡,补偿不同工件的不同内径与底板之间的差别,形成在高度以及在直径上的通用性;When the utility model is used, it is used in conjunction with the installation auxiliary components. After compensating for dimensions such as height and diameter, the workpiece is installed in the tooling and then transferred to each station of electroplating. In cooperation, different workpieces do not need to replace the anode, so there is no need to stop the production line. The replacement of different workpieces can be directly installed in the tool and placed in the electroplating device. The matching installation auxiliary components can also form a transition between the workpiece and the electroplating device. , compensating for the difference between the different inner diameters of different workpieces and the bottom plate, forming the versatility in height and diameter;
安装辅助组件可采用圆筒形结构,在高度上与工件相配合,使得总高度与阳极高度相配合,并且该圆筒形结构的内径为变径,适应于底板与工件之间的过渡安装,在此不再赘述;当然,安装辅助组件的结构并不必然为圆筒形,可以为实现上述目的的任何形状,在此不再赘述;The installation auxiliary component can adopt a cylindrical structure, which is matched with the workpiece in height, so that the total height is matched with the height of the anode, and the inner diameter of the cylindrical structure is variable diameter, which is suitable for the transitional installation between the bottom plate and the workpiece. I will not repeat them here; of course, the structure of the installation auxiliary assembly is not necessarily a cylindrical shape, and can be any shape to achieve the above purpose, and I will not repeat it here;
压紧组件安装于固定架,用于对工件以及安装辅助组件形成压紧,保证工件在运输时以及电镀过程中的稳固性,从而保证电度质量以及电镀过程的顺利进行。The pressing component is installed on the fixing frame, which is used to form a pressing on the workpiece and the installation auxiliary components, so as to ensure the stability of the workpiece during transportation and the electroplating process, so as to ensure the electrical quality and the smooth progress of the electroplating process.
进一步,所述框架具有固定的上纵梁,所述压紧组件设置于上纵梁,并设有可被驱动的上下往复运动的压紧部用于压紧或释放工件;该结构可采用现有的任何机械结构,包括手动或者电动均可,采用现有的机械结构即可实现,在此不再赘述;如图所说,框架包括四个可拆卸式(螺栓)固定在底板上的立柱,纵向两侧(按照多个工件排列的方向)分别设置两个立柱,该两个立柱的上部之间固定连接(螺栓)有上横梁,则所述上纵梁固定连接在两个上横梁之间,形成固定连接的稳定结构,在此不再赘述。Further, the frame has a fixed upper longitudinal beam, the pressing component is arranged on the upper longitudinal beam, and is provided with a pressing part that can be driven to reciprocate up and down for pressing or releasing the workpiece; Any mechanical structure, including manual or electric, can be realized by using the existing mechanical structure, which will not be repeated here; as shown in the figure, the frame includes four detachable (bolt) uprights fixed on the bottom plate , two vertical columns are respectively arranged on both sides of the longitudinal direction (according to the direction of the arrangement of multiple workpieces), and the upper parts of the two columns are fixedly connected (bolts) with an upper beam, then the upper longitudinal beam is fixedly connected between the two upper beams. In the meantime, a stable structure of fixed connection is formed, which is not repeated here.
进一步,所述压紧组件包括可被驱动的沿上纵梁上下往复运动的压紧杆和用于驱动压紧杆往复运动的杠杆组件,所述压紧部位于压紧杆下端;所述杠杆组件包括驱动杠杆和摇臂,所述杠杆阻力端可转动的铰接于压紧杆上端,摇臂下端可相对上纵梁单自由度转动,上端与驱动杠杆的支点可单自由度转动的同轴铰接;所述摇臂上设有限位块,所述限位块在驱动杠杆驱动压紧杆压紧工件时限制杠杆继续向压紧方向转动从而实现锁定;Further, the pressing assembly includes a pressing rod that can be driven to reciprocate up and down along the upper longitudinal beam and a lever assembly for driving the pressing rod to reciprocate, and the pressing part is located at the lower end of the pressing rod; the lever The assembly includes a driving lever and a rocker arm, the resistance end of the lever is rotatably hinged to the upper end of the pressing rod, the lower end of the rocker arm can rotate with a single degree of freedom relative to the upper longitudinal beam, and the upper end and the fulcrum of the driving lever can rotate coaxially with a single degree of freedom. Hinged; a limit block is provided on the rocker arm, and the limit block restricts the lever to continue to rotate in the pressing direction when the driving lever drives the pressing rod to press the workpiece to achieve locking;
压紧杆的往复运动一般为单自由度即只进行往复移动,压紧部可与压紧杆一体成形也可以是分体可拆卸设置,所述压紧部为板状结构的压紧板,一般采用与压紧杆端部呈具有一定自由度的活动连接,比如球绞等活动头,以利于适应压紧端面,保证工件的同轴度;The reciprocating motion of the pressing rod is generally a single degree of freedom, that is, only reciprocating movement. The pressing part can be integrally formed with the pressing rod or can be disassembled separately. Generally, a movable connection with the end of the compression rod with a certain degree of freedom is used, such as a movable head such as a ball twist, so as to adapt to the compression end face and ensure the coaxiality of the workpiece;
摇臂上端通过支点铰接轴与驱动杠杆的支点处铰接,驱动杠杆在外力作用下绕支点转动使得阻力臂由横向趋近于竖直,由此驱动压紧杆下行压紧工件,所述摇臂在压紧杆横向(没有位移)约束下绕其下端向前摆动,在阻力臂压紧工件时所述支点轴线至少与支点铰接轴线相交或者向后超过铰接轴线,由此形成自锁,避免杠杆在反作用力下回转,同时,限位块限制杠杆继续向压紧方向转动,避免继续转动从而驱动压紧杆上行,形成压紧自锁(即压紧杆和驱动杠杆组成的机械结构类似于连杆曲柄结构,但由于被限位块进行限位,避免形成类似于连杆曲柄的圆周运动,从而形成自锁)。The upper end of the rocker arm is hinged with the fulcrum of the driving lever through the pivot hinge shaft, and the driving lever rotates around the pivot point under the action of external force, so that the resistance arm tends to be vertical from the lateral direction, thereby driving the pressing rod downward to press the workpiece, the rocker arm Under the lateral (no displacement) constraint of the pressing rod, it swings forward around its lower end. When the resistance arm presses the workpiece, the fulcrum axis at least intersects with the fulcrum hinge axis or exceeds the hinge axis backward, thereby forming self-locking and avoiding levers It rotates under the reaction force, and at the same time, the limit block restricts the lever to continue to rotate in the pressing direction, so as to avoid continuing to rotate, so as to drive the pressing rod upward, forming a self-locking pressing (that is, the mechanical structure composed of the pressing rod and the driving lever is similar to a connecting rod). Rod crank structure, but because it is limited by the limit block, it avoids the formation of a circular motion similar to the connecting rod crank, thereby forming self-locking).
进一步,所述压紧组件还包括基座,所述基座固定于所述上纵梁,所述压紧杆可单自由度上下往复运动的设置于基座,所述摇臂为两个分列于基座两侧且下端同轴铰接于基座;所述压紧杆通过压紧部压紧工件时,所述压紧杆的轴线相交于或向后超过所述支点的轴线,此时,所述限位块从背侧抵住所述驱动杠杆的阻力臂;Further, the pressing assembly also includes a base, the base is fixed on the upper longitudinal beam, the pressing rod can be arranged on the base to reciprocate up and down with a single degree of freedom, and the rocker arm is divided into two parts. Arranged on both sides of the base and the lower end is coaxially hinged to the base; when the pressing rod presses the workpiece through the pressing part, the axis of the pressing rod intersects or exceeds the axis of the fulcrum backward, at this time , the limit block is pressed against the resistance arm of the drive lever from the back side;
进一步,所述基座可拆卸式固定连接于上纵梁,所述驱动杠杆为以支点为界的直角结构,阻力臂形成叉形槽且压紧杆位于叉形槽内铰接于阻力臂端部,叉形结构利于稳定连接且不施加偏向力,从而使结构稳定且寿命周期较长;如图所示,驱动杠杆为以支点为界的直角结构,即在支点处转角,动力臂向前折弯,方便操作且与摇臂(限位块)不发生干扰;Further, the base is detachably and fixedly connected to the upper longitudinal beam, the driving lever is a right-angle structure bounded by a fulcrum, the resistance arm forms a fork-shaped groove, and the pressing rod is located in the fork-shaped groove and is hinged to the end of the resistance arm , the fork-shaped structure is conducive to stable connection and does not apply biasing force, so that the structure is stable and has a long life cycle; as shown in the figure, the driving lever is a right-angle structure bounded by a fulcrum, that is, at the fulcrum, the power arm folds forward Curved, easy to operate and does not interfere with the rocker arm (limit block);
本实用新型中的向后指的是驱动杠杆在压紧工件时动力臂摆动的方向,背侧则是与向后相对应的一侧,在此不再赘述。The backward in the present invention refers to the direction in which the power arm swings when the driving lever presses the workpiece, and the back side is the side corresponding to the backward, which will not be repeated here.
由于限位块的作用,杠杆的阻力壁被阻止继续转动,摇臂也在限位块的作用下无法继续转动,即形成互锁,并且所述压紧杆的轴线相交于或向后超过所述支点的轴线(一般为相交即可),即形成稳定的缩进机构,避免松脱。Due to the action of the limit block, the resistance wall of the lever is prevented from continuing to rotate, and the rocker arm cannot continue to rotate under the action of the limit block, that is, an interlock is formed, and the axis of the pressing rod intersects or exceeds the limit The axis of the fulcrum (generally it is enough to intersect), that is, a stable retraction mechanism is formed to avoid loosening.
进一步,所述基座包括有基座板和导向套,上纵梁上开有供压紧杆通过的过孔;所述导向套具有导向滑道且固定于基座板,所述导向滑道正对所述上纵梁上的过孔竖直设置且所述压紧杆穿过导向滑道并与其沿上下可往复运动的配合;基座板与上纵梁之间可拆卸式固定连接;两个摇臂的下端分别对称铰接在导向套的两侧;基座板与上纵梁通过连接孔(螺栓穿过,一般采用腰型孔)可拆卸式连接,具有较强的适应性;导向套通过螺纹连接固定于基座板,结构简单;如图所示,导向套下端加工外螺纹,旋在基座板上的内螺纹上形成连接,为避免脱出,还利用锁紧螺母进行锁紧;摇臂下端铰接在导向套上,结构简单实用,整个锁紧组件形成一个模块,铰接部位完全加工完毕后再安装在基座板上;Further, the base includes a base plate and a guide sleeve, and the upper longitudinal beam is provided with a through hole for the pressing rod to pass through; the guide sleeve has a guide slide and is fixed on the base plate, and the guide slide The via hole on the upper longitudinal beam is vertically arranged, and the pressing rod passes through the guide slideway and cooperates with it to reciprocate up and down; the base plate and the upper longitudinal beam are detachably and fixedly connected; The lower ends of the two rocker arms are symmetrically hinged on both sides of the guide sleeve; the base plate and the upper longitudinal beam are detachably connected through connecting holes (bolts pass through, generally using waist-shaped holes), which has strong adaptability; guide The sleeve is fixed on the base plate by threaded connection, and the structure is simple; as shown in the figure, the lower end of the guide sleeve is machined with external threads, which are screwed on the internal threads of the base plate to form a connection. ;The lower end of the rocker arm is hinged on the guide sleeve, the structure is simple and practical, the whole locking assembly forms a module, and the hinged part is completely processed and then installed on the base plate;
进一步,所述底板上设有用于将底板定位放置于电镀装置的定位孔以及用于安装工件的功能孔,功能孔可为底板通道,用于安装支撑工件的部件,在此不再赘述。Further, the bottom plate is provided with a positioning hole for positioning the bottom plate on the electroplating device and a functional hole for installing the workpiece.
本实用新型的有益效果:本实用新型的用于缸体槽外电镀的工件固定装置,使得工件固定安装于本实用新型后被移送至电镀的各个工位,形成模块式固定,方便更换,配合以安装辅助机构,具有较强的适应性,不同的工件不需更换阳极,因而也不需停止生产线,;实用新型用于缸体槽外电镀具有模块化以及通用性,适合于各种尺寸的工件,实现产品的“无缝切换”,避免停线的产能损失,迅速满足交付需求,将成熟产品的切换时间减至最小,将产能损失降到最低。Beneficial effects of the utility model: The workpiece fixing device used for electroplating outside the cylinder groove of the utility model enables the workpiece to be fixedly installed in the utility model and then moved to each station of electroplating, forming a modular fixation, which is convenient for replacement and cooperates with each other. With the installation auxiliary mechanism, it has strong adaptability. Different workpieces do not need to replace the anode, so there is no need to stop the production line. Workpieces, to achieve "seamless switching" of products, avoid production capacity loss due to line stoppage, quickly meet delivery requirements, minimize the switching time of mature products, and minimize production capacity loss.
附图说明Description of drawings
下面结合附图和实施例对本实用新型作进一步描述。The present utility model will be further described below in conjunction with the accompanying drawings and embodiments.
图1为本实用新型立体图(安装在装置上);Fig. 1 is the perspective view of the utility model (installed on the device);
图2为图1A处放大图;Fig. 2 is an enlarged view at Fig. 1A;
图3为本实用新型的结构剖视图;Fig. 3 is the structural sectional view of the utility model;
图4为图3B处放大图。FIG. 4 is an enlarged view of FIG. 3B .
具体实施方式Detailed ways
图1为本实用新型立体图(安装在装置上),图2为图1A处放大图,图3 为本实用新型的结构剖视图,图4为图3B处放大图,如图所示:下面以使用状态描述本实用新型,本实施例的用于缸体槽外电镀的工件固定装置,包括固定架和压紧组件1;Fig. 1 is a perspective view of the utility model (installed on the device), Fig. 2 is an enlarged view of Fig. 1A, Fig. 3 is a sectional view of the structure of the utility model, Fig. 4 is an enlarged view of Fig. 3B, as shown in the figure: State description The utility model, the workpiece fixing device for electroplating outside the cylinder groove of this embodiment, includes a fixing frame and a
所述固定架包括底板2和固定于底板的框架;The fixing frame includes a base plate 2 and a frame fixed to the base plate;
本实用新型使用时,配合以安装辅助组件用于安装工件并在高度上和直径上补偿后安装在所述底板并通过压紧组件1压紧,且所述安装辅助组件还用于将电镀液导入缸体并用于通过阳极;工件安装于工装后被移送至电镀的各个工位,通过与工件配套的安装辅助组件调整总体高度与阳极形成配合,不同的工件9不需更换阳极,因而也不需停止生产线,更换不同的工件直接安装于本工装且安放于电镀装置即可,配套的安装辅助组件还能在工件与电镀装置之间形成过渡,补偿不同工件的不同内径与底板之间的安装差别,形成在高度以及在直径上的通用性;When the utility model is used, it is matched with an installation auxiliary component for installing the workpiece, and after compensation in height and diameter, it is installed on the bottom plate and pressed by the
安装辅助组件可采用圆筒形结构,在高度上与工件9相配合,使得总高度与阳极高度相配合,并且该圆筒形结构的内径为变径,适应于底板与工件内径之间的过渡,在此不再赘述;当然,安装辅助组件的结构并不必然为圆筒形,可以为实现上述目的的任何形状,在此不再赘述;The installation auxiliary component can adopt a cylindrical structure, which is matched with the workpiece 9 in height, so that the total height is matched with the height of the anode, and the inner diameter of the cylindrical structure is variable diameter, which is suitable for the transition between the bottom plate and the inner diameter of the workpiece , which will not be repeated here; of course, the structure of the installation auxiliary assembly is not necessarily a cylindrical shape, and can be any shape to achieve the above purpose, and will not be repeated here;
压紧组件安装于固定架,用于对工件以及安装辅助组件形成压紧,保证工件在运输时以及电镀过程中的稳固性,从而保证电度质量以及电镀过程的顺利进行。The pressing component is installed on the fixing frame, which is used to form a pressing on the workpiece and the installation auxiliary components, so as to ensure the stability of the workpiece during transportation and the electroplating process, so as to ensure the electrical quality and the smooth progress of the electroplating process.
本实用新型在使用时,所述安装辅助组件包括变径补偿件3,所述变径补偿件3为具有轴向过孔的柱体且可定位安装于底板且将底板与电镀环境绝缘,所述轴向过孔与工件内孔相通用于通过阳极并引入电镀液;不同的所述变径补偿件3 下端具有相同的外形尺寸,上端具有与对应工件内径相适应的内径尺寸,且所述变径补偿件安装工件后的总高度能够与阳极配合完成电镀,使用时,所述工件被压紧组件轴向压紧于所述变径补偿件;When the utility model is in use, the installation auxiliary component includes a diameter reducing compensator 3, which is a cylinder with an axial through hole and can be positioned and installed on the bottom plate and insulates the bottom plate from the electroplating environment, so the The axial through hole is communicated with the inner hole of the workpiece for passing through the anode and introducing the electroplating solution; the lower end of the different reducing compensator 3 has the same outer dimension, and the upper end has the inner diameter size adapted to the inner diameter of the corresponding workpiece, and the The total height of the reducing compensator after the workpiece is installed can be matched with the anode to complete electroplating, and when in use, the workpiece is axially pressed against the reducing compensator by the pressing component;
所述底板上设有用于将底板定位放置于电镀装置的定位孔以及用于安装工件的功能孔,功能孔可为底板通道,用于安装支撑工件的部件;不同高度及直径的工件(气缸)配备不同高度的变径补偿件,使得安装于本发明的工件总高度不变,均能与阳极高度相配合;如图所示,不同的变径补偿件(与不同工件相配合的变径补偿件也不同)下端的固定不变的直径尺寸可以与标准的工装配合安装,上端与对应的工件内径相对应(同径同心),下端用于穿过与底板的底板通道(功能孔)配合(使底板与电镀环境隔绝),上部与工件相配合(不同的工件配合尺寸具有差异),所述变径补偿件安装工件后的总高度使得使用时够与阳极高度相适应完成电镀,使得本装置具有通用性;变径补偿件3采用玻璃钢材料制成(当然也可采用其他具有一定强度的非导电材料,在此不再赘述),具有绝缘效果,提高电镀效率。The bottom plate is provided with a positioning hole for positioning the bottom plate on the electroplating device and a functional hole for installing the workpiece. The functional hole can be a bottom plate channel for installing the components supporting the workpiece; workpieces (cylinders) of different heights and diameters Equipped with variable diameter compensators of different heights, so that the total height of the workpiece installed in the present invention remains unchanged and can be matched with the height of the anode; The fixed and constant diameter of the lower end can be installed with standard tooling, the upper end corresponds to the inner diameter of the corresponding workpiece (concentric with the same diameter), and the lower end is used to pass through the bottom plate channel (functional hole) of the bottom plate to match ( The bottom plate is isolated from the electroplating environment), the upper part is matched with the workpiece (different workpieces have different matching sizes), and the total height of the reducing compensator after the workpiece is installed makes it suitable for use with the anode height to complete the electroplating, so that the device It is versatile; the variable diameter compensator 3 is made of FRP material (of course, other non-conductive materials with certain strength can also be used, which will not be repeated here), which has an insulating effect and improves the electroplating efficiency.
本实施例中,所述安装辅助组件还包括屏蔽件,所述屏蔽件包括由非金属导电材料制成的上屏蔽环7和下屏蔽环10,所述下屏蔽环10同轴嵌入所述变径补偿件3的轴向过孔且轴向与工件9下端同径相抵,所述上屏蔽环7与工件9上端同径相抵并由压紧组件1轴向压紧;所述变径补偿件由非导电材料制成,保证导电部位形成稳定的电镀工况,避免材料的浪费以及对电镀工况的干扰;同径相抵指的是上屏蔽环7内径和下屏蔽环10内径与工件9内径相同且同轴,在电镀过程中,将电镀过程中所产生的边缘毛刺引向上屏蔽环的上边缘和下屏蔽环的下边缘,以保证电镀质量,上屏蔽环7和下屏蔽环10均为导电材料制成,在此不再赘述;当然,上屏蔽环7和下屏蔽环10与工件9(缸体)之间需形成径向密封,以防电镀液外泄;结构上在上屏蔽环7的下端面(与缸体的上端面相接触抵紧) 和下屏蔽环10的上端面(与缸体的下端面相接触抵紧)分别设有密封圈12、13 (可在相应的端面上设置环形密封圈槽,用于放置密封圈),密封圈的材质一般为耐酸碱氟橡胶,通过外力压紧变形即可实现密封以及接触抵紧的目的;所述上屏蔽环的内圆下端形成环形倒角,所述下屏蔽环的内圆上端形成环形倒角,倒角结构可引导毛刺向突变处生长,避免对缸体电镀的干扰,同时,该结构还利于保证不对电镀液的流动形成干扰;上屏蔽环和下屏蔽环采用由非金属导电材料(比如导电橡胶或者塑料)制成,实际使用时,利用较小的外力即可使内镀层与上屏蔽环和下屏蔽环分离(因为非金属导电材料一般与金属镀层的结合力较小),比如用尖锐工具直接剥离,或者利用较小的外力使上屏蔽环和下屏蔽环变形而使镀层剥离,可通过使用具有设定弹性模量的非金属导电材料制作,的该弹性模量的非金属导电材料可通过较小的外力(比如手握)即发生变形,但还能够承受电镀时工件的压紧力,保证电镀过程的顺利进行,从而使得屏蔽环内圆的镀层和毛刺与屏蔽环内圆脱离,屏蔽环可二次使用,同时,内圆的镀层和毛刺可回收,降低消耗及电镀成本;而金属屏蔽环(一般为铝)镀层以及毛刺与屏蔽环结合紧密,无法脱落,采用化学去镀层的方式进行处理,需要提供去镀场地,并且屏蔽环多次去镀后会影响后期使用而报废,镀层也无法回收而随着废液排放,造成极大的浪费。In this embodiment, the auxiliary installation assembly further includes a shielding member, and the shielding member includes an upper shielding ring 7 and a
本实施例中,所述上屏蔽环和下屏蔽环均由POM(聚甲醛)材料添加碳粉制成,添加比例按质量分数小于等于1%,优选0.4%左右,具有较好的物理特性和化学特性,具有较好的导电性且镀层易于脱落,可长期使用而不更换,节约电镀成本。In this embodiment, the upper shielding ring and the lower shielding ring are both made of POM (polyoxymethylene) material added with carbon powder, and the addition ratio is less than or equal to 1% by mass fraction, preferably about 0.4%, which has good physical properties and It has good electrical conductivity and the coating is easy to fall off. It can be used for a long time without replacement, saving the cost of electroplating.
本实施例中,所述安装辅助组件还包括定位套8,所述定位套8上安装有与工件9上的安装螺纹孔配合的定位销801并通过定位销801定位使得定位套与工件同心,所述上屏蔽环7同心置于定位套8内并通过定位套8与工件9同心同径配合;In this embodiment, the installation auxiliary assembly further includes a positioning sleeve 8, on which is installed a
工件9上的安装螺纹孔指的是工件端面自带的螺纹孔,定位套的目的是利用定位销和安装螺纹孔(定位销插入螺纹孔形成定位)之间的配合,保证定位套8 与工件同心,上屏蔽环7安装于定位套内圆从而与工件形成同径同轴配合;定位销一般至少为两个,本实施例即为对称设置的两个,保证定位精度。The installation threaded hole on the workpiece 9 refers to the threaded hole on the end face of the workpiece. The purpose of the positioning sleeve is to use the matching between the positioning pin and the installation threaded hole (the positioning pin is inserted into the threaded hole to form positioning) to ensure the positioning sleeve 8 and the workpiece. Concentric, the upper shielding ring 7 is installed on the inner circle of the positioning sleeve to form the same diameter and coaxial matching with the workpiece; there are generally at least two positioning pins, and this embodiment is two symmetrically arranged to ensure positioning accuracy.
具体安装过程是:将变径补偿件3定位放置于底板2(可用密封圈,该处密封圈可采用EVA泡棉),将下屏蔽环10放置于变径补偿件3,下端与变径补偿件 3之间也可设置密封(密封方式不限)并将密封圈放置于下屏蔽环10的上端面设定位置,在下屏蔽环上放置工件,通过定位套定位后放置上屏蔽环,通过压紧装置压紧即可。The specific installation process is as follows: position the variable diameter compensator 3 on the bottom plate 2 (a sealing ring can be used, and the sealing ring can be made of EVA foam), place the
本实施例中,所述框架具有固定的上纵梁6,所述压紧组件1设置于上纵梁 6,并设有可被驱动的上下往复运动的压紧部5用于压紧或释放工件9;该结构可采用现有的任何机械结构,包括手动或者电动均可,采用现有的机械结构即可实现,在此不再赘述;如图所说,框架包括四个可拆卸式(螺栓)固定在底板2 上的立柱4,纵向两侧(按照多个工件排列的方向)分别设置两个立柱4,该两个立柱4的上部之间固定连接(螺栓)有上横梁12,则所述上纵梁6固定连接在两个上横梁12之间,形成固定连接的稳定结构,在此不再赘述。In this embodiment, the frame has a fixed upper
本实施例中,所述压紧组件1包括可被驱动的沿上纵梁6上下往复运动的压紧杆101和用于驱动压紧杆101往复运动的杠杆组件,所述压紧部5位于压紧杆 101下端;所述杠杆组件包括驱动杠杆(包括动力臂1021和阻力臂1022)和摇臂,所述杠杆阻力端(即阻力臂的端部)可转动的铰接于压紧杆101上端,摇臂下端可相对上纵梁单自由度转动,上端与驱动杠杆的支点可单自由度转动的同轴铰接;所述摇臂上设有限位块104,所述限位块104在驱动杠杆驱动压紧杆101 压紧工件时限制杠杆继续向压紧方向转动;In this embodiment, the
压紧杆101的往复运动一般为单自由度即只进行往复移动,压紧部5可与压紧杆101一体成形也可以是分体可拆卸设置,本实施例中采用板状结构的压紧部,一般采用与压紧杆端部呈具有一定自由度的活动连接,比如球绞等活动头,以利于适应压紧端面,保证工件的同轴度;The reciprocating motion of the
摇臂上端通过支点铰接轴14与驱动杠杆的支点处铰接,驱动杠杆在外力作用下绕支点转动使得阻力臂1022由横向趋近于竖直,由此驱动压紧杆101下行压紧工件,所述摇臂在压紧杆101横向(没有位移)约束下绕摇臂下端铰接点向前摆动,在阻力臂1022压紧工件时所述支点轴线至少与支点铰接轴线(铰接轴 14的轴线)相交或者向后超过铰接轴线,由此形成自锁,避免杠杆在反作用力下回转,同时,限位块限制杠杆继续向压紧方向转动,避免继续转动从而驱动压紧杆上行,形成压紧自锁(即压紧杆和驱动杠杆组成的机械结构类似于连杆曲柄结构,但由于被限位块进行限位,避免形成类似于连杆曲柄的圆周运动,从而形成自锁)。The upper end of the rocker arm is hinged with the fulcrum of the driving lever through the
本实施例中,所述压紧组件1还包括基座,所述基座固定于所述上纵梁6,所述压紧杆101可单自由度上下往复运动的设置于基座,所述摇臂为两个分列于 (摇臂1031和摇臂1032)基座两侧且下端同轴铰接于基座,上端分别同轴铰接于驱动杠杆的支点的两侧(即与驱动杠杆在支点处同轴转动);所述压紧杆101 通过压紧部压紧工件时,所述压紧杆的轴线相交于或向后超过所述支点的轴线,此时,所述限位块从背侧抵住所述驱动杠杆的阻力臂;In this embodiment, the
如图所示,基座通过可拆卸式结构固定于上纵梁6表面,上纵梁6上开有供压紧杆通过的过孔;基座包括有基座板105和导向套107,导向套具有导向滑道,所述导向滑道正对所述上纵梁上的过孔竖直设置且所述压紧杆穿过导向滑道并与其沿上下可往复运动的配合;基座板105与上纵梁6通过连接孔(螺栓穿过,一般采用腰型孔)可拆卸式连接,具有较强的适应性;导向套107通过螺纹连接固定于基座板105,结构简单;如图所示,导向套107下端加工外螺纹,以轴线 (导向滑道的方向)垂直于基座板105的方式旋在基座板105上的内螺纹上形成连接,为避免脱出,还利用锁紧螺母106进行锁紧;所述压紧杆沿竖直方向穿过导向套107并与其往复运动配合(一般为单自由度);摇臂1031下端和摇臂1032 下端分别对称铰接在导向套107的两侧,结构简单实用,整个锁紧组件形成一个模块,铰接部位完全加工完毕后再安装在基座板上;As shown in the figure, the base is fixed on the surface of the upper
本实用新型中的向后指的是驱动杠杆在压紧工件时动力臂1022摆动的方向 (图4箭头所指方向),背侧则是与向后相对应的一侧,在此不再赘述。In the present invention, backward refers to the direction in which the
由于限位块14的作用,杠杆的阻力壁1022被阻止继续转动,摇臂1031和摇臂1031也在限位块的作用下无法继续转动,即形成互锁,并且所述压紧杆的轴线相交于或向后超过所述支点的轴线(一般为相交即可),即形成稳定的缩进机构,避免松脱。Due to the action of the
本实施例中,所述基座可拆卸式固定连接于上纵梁6,所述驱动杠杆为以支点为界的直角结构,阻力臂1022形成叉形槽且压紧杆101位于叉形槽内铰接于阻力臂端部,叉形结构利于稳定连接且不施加偏向力,从而使结构稳定且寿命周期较长;如图所示,驱动杠杆为以支点为界的直角结构(即动力臂1021与阻力臂1022呈直角),即在支点处转角,动力臂向前折弯,方便操作且与摇臂(限位块)不发生干扰。In this embodiment, the base is detachably and fixedly connected to the upper
本实施例中,所述工件9与上屏蔽环7和下屏蔽环10之间抵紧接触且形成径向密封,径向密封指的是在端面上设置密封圈,防止液体从径向上泄漏。In this embodiment, the workpiece 9 is in close contact with the upper shielding ring 7 and the
本实施例中,所述变径补偿件3可定位的安装于底板2且与底板通道201同轴,且内圆设有用于安放下屏蔽环10的台阶,所述台阶内径尺寸大于下屏蔽环 10的内径,保证电镀液的稳定流动;所述上屏蔽环7同轴置于定位套8的内圆,所述压紧组件1通过上屏蔽环7压紧工件9;变径补偿件3可定位的安装于底板 2可采用多种机械结构,比如在底板通道201(形状与变径补偿件径向的外形尺寸相同,本实施例为圆形)上形成环形沉槽,变径补偿件置于环形沉槽,形成横向的定位即达到同轴的效果,也可以采用如图所示的变径补偿件通过轴肩(阶梯轴)结构与底板通道相配合,即小直径部分穿过底板通道,大直径部分的轴肩压在底板通道的边沿,形成定位;In this embodiment, the variable diameter compensator 3 can be positioned and installed on the bottom plate 2 and is coaxial with the
与工件(缸体)直接接触的部位密封一般采用耐酸碱氟橡胶密封圈,如上下屏蔽环与工件之间的密封,确保密封同时,能保障屏蔽圈与工件缸体之间的紧密接触以成功转移毛刺;而不与工件发生直接接触的密封则采用EVA泡棉(比如下屏蔽环与变径补偿件之间等),以减少操作者放置/取出胶圈的装夹动作,提高装夹效率;如图所示,工件安装于本实用新型后,将本实用新型的工装移至电镀装置上通过定位孔空202与装置11上的定位凸起1101配合,保证安置位置与装置的电镀液流道配合,保证电镀的正常进行。The parts in direct contact with the workpiece (cylinder) are generally sealed with acid and alkali-resistant fluororubber sealing rings, such as the sealing between the upper and lower shielding rings and the workpiece, to ensure the sealing and at the same time, it can ensure the close contact between the shielding ring and the workpiece cylinder to prevent The burr is successfully transferred; the seal without direct contact with the workpiece is made of EVA foam (such as between the lower shielding ring and the reducing compensator, etc.) Efficiency; as shown in the figure, after the workpiece is installed in the present utility model, the tooling of the present utility model is moved to the electroplating device through the
本发明的槽外电镀指的是通过在电镀液槽外形成电镀液循环而实现的动态电镀,在此不再赘述。The electroplating outside the tank of the present invention refers to the dynamic electroplating realized by forming the electroplating liquid circulation outside the electroplating liquid tank, and details are not repeated here.
本实施例是以发动机缸体为例,实际上本发明所要求保护的技术方案并不局限于发动机缸体,还可以是压缩机气缸、柱塞泵缸体等等具有相似结构的缸体,在此不再赘述。This embodiment takes an engine cylinder block as an example. In fact, the technical solution claimed in the present invention is not limited to an engine cylinder block, but can also be a cylinder block of a compressor cylinder, a piston pump cylinder block, etc. with similar structures, It is not repeated here.
最后说明的是,以上实施例仅用以说明本实用新型的技术方案而非限制,尽管参照较佳实施例对本实用新型进行了详细说明,本领域的普通技术人员应当理解,可以对本实用新型的技术方案进行修改或者等同替换,而不脱离本实用新型技术方案的宗旨和范围,其均应涵盖在本实用新型的权利要求范围当中。Finally, it should be noted that the above embodiments are only used to illustrate the technical solutions of the present invention and not to limit them. Although the present invention has been described in detail with reference to the preferred embodiments, those of ordinary skill in the art should The technical solutions are modified or equivalently replaced without departing from the purpose and scope of the technical solutions of the present invention, and all of them should be included in the scope of the claims of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922177969.7U CN211734510U (en) | 2019-12-06 | 2019-12-06 | Workpiece fixing device for electroplating outside cylinder body tank |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922177969.7U CN211734510U (en) | 2019-12-06 | 2019-12-06 | Workpiece fixing device for electroplating outside cylinder body tank |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN211734510U true CN211734510U (en) | 2020-10-23 |
Family
ID=72875388
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201922177969.7U Expired - Fee Related CN211734510U (en) | 2019-12-06 | 2019-12-06 | Workpiece fixing device for electroplating outside cylinder body tank |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN211734510U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112593272A (en) * | 2020-11-30 | 2021-04-02 | 中国航发动力股份有限公司 | Clamping tool |
-
2019
- 2019-12-06 CN CN201922177969.7U patent/CN211734510U/en not_active Expired - Fee Related
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112593272A (en) * | 2020-11-30 | 2021-04-02 | 中国航发动力股份有限公司 | Clamping tool |
| CN112593272B (en) * | 2020-11-30 | 2021-09-21 | 中国航发动力股份有限公司 | Clamping tool |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN211734520U (en) | Circulating electroplating system of cylinder body | |
| CN110886004B (en) | Electroplating device for electroplating outside cylinder body tank | |
| CN113878184B (en) | Multifunctional electrolytic machining process device for hole and groove structures | |
| CN110923789B (en) | Electroplating environment treatment device for electroplating outside cylinder body tank | |
| CN203546167U (en) | Oil cylinder barrel brush electroplating restoration test platform | |
| CN110760909A (en) | Universal tooling for plating out of cylinder tanks | |
| CN211734509U (en) | Universal compensation device for circular electroplating | |
| CN110923790B (en) | Compensating Auxiliary Tooling for Out-of-Cylinder Slot Plating | |
| CN211734517U (en) | Universal clamping device for circular electroplating of cylinder body | |
| CN211734508U (en) | Circulating electroplating device for cylinder body | |
| CN110886005B (en) | Anode assembly for cylinder body outside-tank electroplating | |
| CN211734519U (en) | Anode device for circular electroplating of cylinder body | |
| CN207873604U (en) | A kind of device of automatic riveting dish valve screw | |
| CN212404332U (en) | Electroplating environment forming tool for cyclic electroplating of cylinder body | |
| CN211227401U (en) | Circulating electroplating shielding assembly of cylinder body | |
| CN110886003B (en) | Shielding structure for electroplating outside cylinder tank | |
| CN223813555U (en) | Universal liquid supply system for automatic electroplating of cylinder holes | |
| CN220659968U (en) | Drilling fixture with drilling lubrication feeding function | |
| CN223823728U (en) | Support frame for general-purpose external plating fixtures for cylinder bores | |
| CN223823719U (en) | Universal external electroplating equipment for cylinder bores | |
| CN210974892U (en) | Cylinder body plating front tool based on communicating vessel principle | |
| CN212495147U (en) | An easy-to-install magnetic flux converter riveting device | |
| CN110760908B (en) | A before plating processing apparatus for cylinder body is electroplated | |
| CN111155155B (en) | Universal type groove external electroplating system for cylinder body | |
| CN223823720U (en) | Universal external plating assembly for cylinder bores |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20201023 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |