Disclosure of Invention
For overcoming the problem that exists in the correlation technique at least to a certain extent, the aim at of this application provides a little semicircle diameter's of axle type part measuring device and method, and it can solve current little semicircle diameter measuring error great, and the computational method is complicated loaded down with trivial details, is unfavorable for the problem of quick accurate detection. The technical effects that can be produced by the preferred technical scheme in the technical schemes provided by the application are described in detail in the following.
The application provides a measuring device for the small semicircular diameter of an axle part, which comprises a dial indicator support, a dial indicator and an indicator sample piece, wherein the dial indicator support comprises a supporting part and an indicator frame plate, the supporting part is provided with a V-shaped groove, the indicator frame plate is connected to the supporting part, and one end far away from the supporting part is provided with a mounting hole for the dial indicator to extend into and a limiting component for fixing the dial indicator in the mounting hole; the two groove walls of the V-shaped groove and the mounting hole are in mirror symmetry relative to a first plane, and the mounting hole and the axis of the dial indicator are located on the first plane; the pair of appearance piece including be used for with the first journal that the cell wall of V type groove contacted with be used for with the second journal that the measuring head of percentage table contacted.
Preferably, the included angle between the two groove walls of the V-shaped groove is 120 degrees.
Preferably, an opening bushing is arranged in the mounting hole, and the limiting assembly comprises an adjusting screw hole communicated with the mounting hole and an adjusting screw which is positioned in the adjusting screw hole and can be in contact with the opening bushing.
Preferably, an installation surface is arranged on one side, far away from the V-shaped groove, of the supporting portion, the installation surface is perpendicular to the first plane, and the meter frame plate is flatly paved and connected on the installation surface.
Preferably, the mounting surface and the watch frame plate are positioned by a positioning pin hole and a positioning pin, and the positioning pin hole is mirror-symmetrical relative to the first plane.
Preferably, the mounting surface and the watch frame plate are connected through connecting screw holes and connecting bolts, and the connecting screw holes and the connecting bolts are symmetrically arranged in multiple groups relative to the first plane.
Preferably, the first journal is larger than the second journal.
The application also provides a method for measuring the diameter of the shaft part small semicircle, which is based on the device for measuring the diameter of the shaft part small semicircle, and comprises the following steps:
obtaining the design sizes of a third shaft neck and a small semicircular shaft neck of a workpiece to be tested according to a design drawing, and processing a first shaft neck and a second shaft neck of the pair of sample pieces according to the design sizes of the third shaft neck and the small semicircular shaft neck, so that the design sizes of the first shaft neck and the third shaft neck are consistent, and the design sizes of the second shaft neck and the small semicircular shaft neck are consistent;
two groove walls of the V-shaped groove are in contact with the first journal, a measuring head of the dial indicator is in contact with the second journal, and the reading of the dial indicator is zeroed;
and two groove walls of the V-shaped groove are in contact with the third shaft neck, the measuring head of the dial indicator is in contact with the small semicircular shaft neck of the workpiece to be measured, the radius difference between the second shaft neck and the small semicircular shaft neck is obtained through reading of the dial indicator and is a preprocessing difference value of the small semicircular shaft neck, and the size of the small semicircular shaft neck is obtained through calculation.
The application also provides a method for measuring the diameter of the shaft part small semicircle, which is based on the device for measuring the diameter of the shaft part small semicircle, and comprises the following steps:
acquiring the size of a third shaft neck at the end part of a workpiece to be detected, and processing the pair of sample pieces according to the size of the third shaft neck, so that the first shaft neck and the third shaft neck have the same size, and acquiring the size of a second shaft neck of the pair of sample pieces;
two groove walls of the V-shaped groove are in contact with the first journal, a measuring head of the dial indicator is in contact with the second journal, and the reading of the dial indicator is zeroed;
two groove walls of the V-shaped groove are in contact with the third journal, a measuring head of the dial indicator is in contact with a small semicircular journal of a workpiece to be measured, and the radius difference between the second journal and the small semicircular journal is a first difference value through reading of the dial indicator;
calculating the size of the small semicircular journal according to the second journal and the first difference.
The technical scheme provided by the application can comprise the following beneficial effects:
when the shaft neck test device is used, the design sizes of a third shaft neck and a small semicircular shaft neck of a workpiece to be tested can be obtained according to a design drawing, and the first shaft neck and the second shaft neck of the sample test piece are processed according to the design sizes of the third shaft neck and the small semicircular shaft neck, so that the size of the first shaft neck is consistent with the design size of the third shaft neck, and the size of the second shaft neck is consistent with the design size of the small semicircular shaft neck; firstly, two groove walls of the V-shaped groove are in contact with the first journal, a measuring head of the dial indicator is in contact with the second journal, and the reading of the dial indicator is zeroed; and then, two groove walls of the V-shaped groove are contacted with the third shaft neck, the measuring head of the dial indicator is contacted with the small semicircular shaft neck of the workpiece to be measured, the radius difference between the second shaft neck and the small semicircular shaft neck is obtained through reading of the dial indicator and is a preprocessing difference value of the small semicircular shaft neck, the actual size of the small semicircular shaft neck of the workpiece to be measured can be obtained through calculation, and the small semicircular shaft neck can be conveniently processed. In another use mode, the end part of the workpiece to be measured is round and forms a third shaft neck, the size can be obtained according to a drawing or measurement, and a pair of sample parts is processed according to the size of the third shaft neck of the workpiece to be measured, so that the size of the first shaft neck of the pair of sample parts is consistent with that of the third shaft neck of the workpiece to be measured, the support positions of the pair of sample parts and the workpiece to be measured in the V-shaped groove are consistent, and the size of the second shaft neck of the pair of sample parts is obtained; when V type groove and first journal contacted, the measuring head and the second journal of percentage table contacted, and then can zero the percentage table, when V type groove and third journal contacted, the measuring head and the little semicircle journal of percentage table contacted, can draw the radius difference that second journal and little semicircle journal are first difference through the percentage table, so, and then calculate the size of getting little semicircle journal according to second journal and first difference. So set up, the frock simple structure of adoption, it is low to operating personnel's requirement, the installation is adjusted conveniently, has reduced calculation and calculation error among the measurement process, has improved measurement of efficiency, can also adapt to the measurement of the little semicircle journal of similar structure, and the measuring mode commonality is high.
It is to be understood that both the foregoing general description and the following detailed description are exemplary and explanatory only and are not restrictive of the application.
Detailed Description
Reference will now be made in detail to the exemplary embodiments, examples of which are illustrated in the accompanying drawings. When the following description refers to the accompanying drawings, like numbers in different drawings represent the same or similar elements unless otherwise indicated. The embodiments described in the following exemplary embodiments do not represent all embodiments consistent with the present application. Rather, they are merely examples of apparatus or methods consistent with aspects of the present application.
In order to make the objects, technical solutions and advantages of the present invention more apparent, the technical solutions of the present invention will be described in detail below. It is to be understood that the described embodiments are merely exemplary of the invention, and not restrictive of the full scope of the invention. All other embodiments, which can be derived by a person skilled in the art from the examples given herein without any inventive step, are within the scope of the present invention.
Hereinafter, embodiments will be described with reference to the drawings. The embodiments described below do not limit the contents of the invention described in the claims. The entire contents of the configurations shown in the following embodiments are not limited to those required as solutions of the inventions described in the claims.
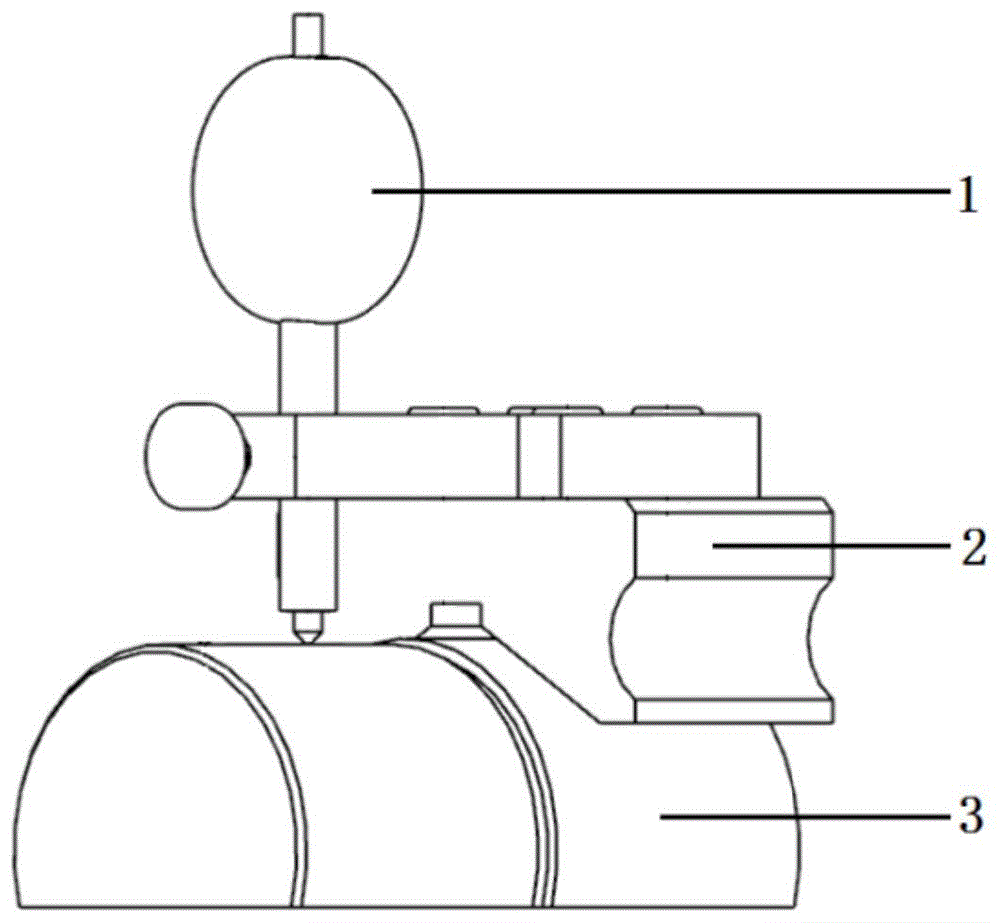
Referring to fig. 1 to 7, the present embodiment provides a device for measuring a small semicircular diameter of an axle part, including a dial indicator support 2, a dial indicator 1 and a sample measuring part 3, wherein the dial indicator support 2 includes a support portion 13 and a frame plate 9, the support portion 13 is provided with a V-shaped groove, and a groove wall of the V-shaped groove can contact with a journal of the sample measuring part 3, so as to compare the workpiece 4 to be measured conveniently; the one end of table frame board 9 is fixed on supporting part 13, the other end is used for connecting percentage table 1, specifically, the tip of table frame board 9 is provided with mounting hole 7 and spacing subassembly, insert percentage table 1 in mounting hole 7 during the installation, adjust to suitable position, spacing subassembly of rethread is fixed percentage table 1 in mounting hole 7, and then realize the rigidity between percentage table 1 and the table frame board 9, here, mounting hole 7 runs through along the direction of perpendicular to table frame board 9, so that the measuring direction of percentage table 1 is perpendicular with table frame board 9.
Here, a plane perpendicular to the frame plate 9 is set as a first plane, wherein both the two groove walls of the V-shaped groove and the mounting hole 7 are mirror-symmetric with respect to the first plane, so that the mounting hole 7 and the axis of the dial indicator 1 are located on the first plane, and thus, when the outer peripheral surface of the sample piece 3 is in contact with the groove walls of the V-shaped groove, the mounting hole 7 extends in the radial direction of the sample piece 3, so that the dial indicator 1 can measure the distance in the radial direction of the sample piece 3, thereby ensuring that the radius difference measured by the dial indicator 1 is accurate and reliable.
The pair of sample parts 3 comprises a first shaft neck 16 and a second shaft neck 15, the sizes of the first shaft neck 16 and the second shaft neck 15 can be consistent, or a difference can exist, and the difference is a fixed value on the basis of not influencing measurement, specifically, when the pair of sample parts 3 is used, the design sizes of a third shaft neck 17 and a small semicircular shaft neck 18 of a workpiece 4 to be measured can be obtained according to a design drawing, and the first shaft neck 16 and the second shaft neck 15 of the pair of sample parts 3 are processed according to the design sizes of the third shaft neck 17 and the small semicircular shaft neck 18, so that the size of the first shaft neck is consistent with the design size of the third shaft neck, and the size of the second shaft neck is consistent with the design size of the small semicircular shaft neck; firstly, two groove walls of the V-shaped groove are in contact with a first journal 16, a measuring head of the dial indicator 1 is in contact with a second journal 15, and the reading of the dial indicator 1 is zeroed; and then two groove walls of the V-shaped groove are contacted with a third shaft neck 17, a measuring head of the dial indicator 1 is contacted with a small semicircular shaft neck 18 of the workpiece 4 to be measured, the radius difference between the second shaft neck 15 and the small semicircular shaft neck 18 is obtained through the reading of the dial indicator 1 and is a preprocessing difference value of the small semicircular shaft neck 18, and meanwhile, the actual size of the small semicircular shaft neck of the workpiece to be measured can be obtained through calculation, so that the small semicircular shaft neck can be conveniently processed.
In another use mode, the end part of the workpiece 4 to be measured is a full circle to form a third journal 17, the size can be obtained according to a drawing or measurement, and a pair of sample parts 3 is processed according to the size of the third journal 17 of the workpiece 4 to be measured, so that the size of the first journal 16 of the pair of sample parts 3 is consistent with that of the third journal 17 of the workpiece 4 to be measured, the supporting positions of the pair of sample parts 3 and the workpiece 4 to be measured in a V-shaped groove are consistent, and the size of the second journal 15 of the pair of sample parts is obtained; when the V-shaped groove is in contact with the first journal 16, the measuring head of the dial indicator 1 is in contact with the second journal 15, the dial indicator 1 can be adjusted to zero, when the V-shaped groove is in contact with the third journal 17, the measuring head of the dial indicator 1 is in contact with the small semicircular journal 18, the radius difference between the second journal 15 and the small semicircular journal 18 can be obtained through the dial indicator 1 and is a first difference value, and therefore the size of the small semicircular journal 18 can be obtained through calculation according to the second journal 15 and the first difference value.
So set up, the frock simple structure of adoption, it is low to operating personnel's requirement, the installation is adjusted conveniently, has reduced calculation and calculation error among the measurement process, has improved measurement of efficiency, can also adapt to the measurement of the little semicircle journal 18 of similar structure, and the measuring method commonality is high.
In this embodiment, the contained angle of two cell walls in V type groove is 120 degrees, like this, is favorable to the embedding to the table appearance piece 3 and the work piece 4 that awaits measuring, and opens the angle suitable, is favorable to promoting diameter measurement's accuracy. The angle of the V-groove can be adapted to the specific size of the first journal 16 of the form part 3.
An opening bushing 8 is arranged in the mounting hole 7, and the opening bushing 8 is arranged between the mounting hole 7 and the dial indicator 1 in a spaced mode, so that buffering and fixing effects can be achieved; spacing subassembly is including adjusting screw 6 and adjusting screw 5, adjusts screw 6 and extends along the extending direction of table skeleton board 9 and link up with mounting hole 7, and adjusting screw 5 is connected in adjusting screw 6 and can contact with opening bush 8 in the mounting hole 7, like this, support opening bush 8 through adjusting screw 5 and support percentage table 1 tightly in mounting hole 7, simple structure, and the simple operation.
In some embodiments, the supporting portion 13 is provided with a mounting surface, the mounting surface and the V-shaped groove are respectively disposed on two opposite side surfaces of the supporting portion 13, the mounting surface is perpendicular to the first plane, and the watch frame plate 9 is flatly connected to the mounting surface, so that the connection manner between the surface and the surface is favorable for improving the stability of the watch frame plate 9 and preventing the watch frame plate 9 from rotating and skewing.
In order to achieve a good positioning effect, the mounting surface and the meter frame plate 9 are positioned through the positioning pin holes 14 and the positioning pins 10, the positioning pin holes 14 are in mirror symmetry relative to the first plane, and the positioning pin holes 14 and the positioning pins 10 are arranged in two groups and are arranged along the extending direction of the first plane, so that the positioning accuracy is guaranteed.
Further, the mounting surface and the meter frame plate 9 are connected through connecting screw holes 11 and connecting bolts 12, specifically, the mounting surface and the meter frame plate 9 are provided with the connecting screw holes 11, the connecting bolts 12 are positioned in the connecting screw holes 11 and connect the mounting surface and the meter frame plate 9, and here, the connecting screw holes 11 and the connecting bolts 12 are symmetrically arranged in multiple groups relative to the first plane, so that the left and right balance and stability of the mounting surface and the meter frame plate 9 relative to the first plane are ensured.
In some preferred schemes, the first journal 16 is larger than the second journal 15 in size, so that a step is formed on the outer peripheral surface of the sample piece 3, and since the small semicircular journal 18 of the workpiece 4 to be measured is smaller than the third journal 17, the sample piece 3 will be correspondingly arranged, which is beneficial to reducing the calculation error.
The following describes the measurement device for the diameter of the small semicircle of the spindle part.
A measuring device for the small semicircular diameter of a shaft part comprises a supporting part 13, a dial indicator 1, a meter sample piece 3, a meter frame plate 9, a positioning pin 10, a connecting bolt 12, an opening bush 8 and an adjusting screw 5; the supporting part 13 is provided with a V-shaped groove and an installation surface, two positioning pin holes 14 and four threaded holes are distributed on the installation surface, two positioning pin holes 14 and four countersunk holes are distributed on the meter frame plate 9, and the installation surface corresponds to the pin holes, the threaded holes and the countersunk holes on the meter frame plate 9 in position, so that the supporting part 13 and the meter frame plate 9 are connected together through the positioning pins 10 and the connecting bolts 12; the other end of the meter frame plate 9 is provided with a mounting hole 7 for mounting the dial indicator 1, an opening bush 8 is embedded in the mounting hole 7, the front end of the meter frame plate 9 is provided with an adjusting screw 5 for fixing the dial indicator 1, and the position of the dial indicator 1 is fixed by a mode that the adjusting screw compresses the opening bush 8.
The application also provides a method for measuring the small semicircular diameter of the shaft part, which comprises the following steps:
obtaining the design sizes of a third shaft neck 17 and a small semicircular shaft neck 18 of a workpiece 4 to be measured according to a design drawing, and processing a first shaft neck 16 and a second shaft neck 15 of a sample piece 3 according to the design sizes of the third shaft neck 17 and the small semicircular shaft neck 18, so that the design sizes of the first shaft neck 16 and the third shaft neck 17 are consistent, and the design sizes of the second shaft neck 15 and the small semicircular shaft neck 18 are consistent;
two groove walls of the V-shaped groove are in contact with the first journal 16, the measuring head of the dial indicator 1 is in contact with the second journal 15, and the reading of the dial indicator 1 is zeroed;
and (3) contacting two groove walls of the V-shaped groove with a third journal 17, contacting a measuring head of the dial indicator 1 with a small semicircular journal 18 of the workpiece 4 to be measured, acquiring a pre-processing difference value of the radius difference between the second journal 15 and the small semicircular journal 18 as the small semicircular journal 18 through the reading of the dial indicator 1, and calculating to obtain the size of the small semicircular journal 18.
After the preprocessing difference value of the small semicircular shaft neck 18 is obtained, the actual size of the small semicircular shaft neck of the workpiece to be measured can be calculated, and the small semicircular shaft neck can be conveniently processed. So set up, the frock simple structure of adoption, it is low to operating personnel's requirement, the installation is adjusted conveniently, has reduced calculation and calculation error among the measurement process, has improved measurement of efficiency, can also adapt to the measurement of the little semicircle journal 18 of similar structure, and the measuring method commonality is high. The derivation process of the beneficial effect is substantially similar to the derivation process of the beneficial effect brought by the mobile base, and therefore, the description is omitted here.
The application also provides a method for measuring the small semicircular diameter of the shaft part, which comprises the following steps:
acquiring the size of a third journal 17 at the end part of the workpiece 4 to be measured, processing the sample 3 according to the size of the third journal 17 to enable the first journal 16 and the third journal 17 to be the same in size, and acquiring the size of a second journal 15 of the sample 3;
two groove walls of the V-shaped groove are in contact with the first journal 16, the measuring head of the dial indicator 1 is in contact with the second journal 15, and the reading of the dial indicator 1 is zeroed;
two groove walls of the V-shaped groove are contacted with a third journal 17, a measuring head of the dial indicator 1 is contacted with a small semicircular journal 18 of the workpiece 4 to be measured, and the radius difference between the second journal 15 and the small semicircular journal 18 is obtained as a first difference value through the reading of the dial indicator 1;
the size of the small semicircular journal 18 is calculated based on the second journal 15 and the first difference.
The following describes the method for measuring the diameter of the small semi-circle of the axial part.
Step one, grinding a first journal 16 and a second journal 15 of a sample part 3 to ensure that the size of the first journal 16 is consistent with that of a third journal 17 of a workpiece 4 to be measured so as to ensure that the support of a V-shaped groove on a support part 13 is consistent with that of the third journal 17 of the actual workpiece 4 to be measured, which is equivalent to the uniform measurement reference;
zeroing the dial indicator 1, supporting the V-shaped groove of the supporting part 13 on the dial indicator piece 3, adjusting the dial indicator 1 by adjusting an adjusting screw 5 at the front end of the dial indicator frame plate 9 to enable a measuring head of the dial indicator 1 to be pressed on a corresponding second journal 15 with proper force, and then rotating a dial plate of the dial indicator 1 to enable the dial plate to read zero;
and thirdly, tightly supporting the V-shaped groove of the supporting part 13 on a third shaft neck 17 of the workpiece 4 to be measured, wherein a measuring head of the dial indicator 1 is just in pressure contact with a small semicircular shaft neck 18 of the workpiece 4 to be measured, and the reading of the dial indicator 1 is the difference value between the small semicircular shaft neck 18 of the workpiece 4 to be measured and a second shaft neck 15 of the sample fitting 3.
So set up, the frock simple structure of adoption, it is low to operating personnel's requirement, the installation is adjusted conveniently, has reduced calculation and calculation error among the measurement process, has improved measurement of efficiency, can also adapt to the measurement of the little semicircle journal 18 of similar structure, and the measuring method commonality is high. The derivation process of the beneficial effect is substantially similar to the derivation process of the beneficial effect brought by the mobile base, and therefore, the description is omitted here.
It should be noted that the terms "first," "second," and the like, as used herein, are not intended to limit the specific order, but merely to distinguish one element or function from another. The stated horizontal, vertical, up, down, left and right are the ones when the measuring device and method for the small semi-circle diameter of the shaft parts are in natural arrangement state.
The above description is only for the specific embodiments of the present invention, but the scope of the present invention is not limited thereto, and any person skilled in the art can easily conceive of the changes or substitutions within the technical scope of the present invention, and the changes or substitutions should be covered within the scope of the present invention. Therefore, the protection scope of the present invention shall be subject to the protection scope of the claims.
It is understood that the same or similar parts in the above embodiments may be mutually referred to, and the same or similar parts in other embodiments may be referred to for the content which is not described in detail in some embodiments. The multiple schemes provided by the application comprise basic schemes of the schemes, are independent of each other and are not restricted to each other, but can be combined with each other under the condition of no conflict, so that multiple effects are achieved together.
While embodiments of the present application have been shown and described above, it is to be understood that the above embodiments are exemplary and not to be construed as limiting the present application, and that changes, modifications, substitutions and alterations may be made to the above embodiments by those of ordinary skill in the art within the scope of the present application.