WO2025083751A1 - エアレスタイヤの製造方法及び製造装置 - Google Patents
エアレスタイヤの製造方法及び製造装置 Download PDFInfo
- Publication number
- WO2025083751A1 WO2025083751A1 PCT/JP2023/037369 JP2023037369W WO2025083751A1 WO 2025083751 A1 WO2025083751 A1 WO 2025083751A1 JP 2023037369 W JP2023037369 W JP 2023037369W WO 2025083751 A1 WO2025083751 A1 WO 2025083751A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- spokes
- force
- tread
- wheel
- ring
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29D—PRODUCING PARTICULAR ARTICLES FROM PLASTICS OR FROM SUBSTANCES IN A PLASTIC STATE
- B29D30/00—Producing pneumatic or solid tyres or parts thereof
- B29D30/02—Solid tyres ; Moulds therefor
Definitions
- the present invention relates to a manufacturing method and manufacturing device for airless tires (also called non-pneumatic tires or non-pneumatic tires).
- An airless tire that has a base connected to a rigid portion, a top that is connected to the tire tread, and a deformable structure provided between the base and the top (Patent Document 1).
- the deformable structure is formed, for example, by injection molding of polyurethane.
- reinforcing material e.g., metal wire
- reinforcing material may be provided in the tread along the circumference of the airless tire to prevent excessive deformation of the spokes.
- a force is applied to the reinforcing material from the inner circumference to the outer circumference of the airless tire, generating tensile stress in the circumferential direction and increasing the rigidity of the reinforcing material.
- airless tires manufactured using the above-mentioned conventional technology have the problem that the force from the base to the tread weakens due to contraction of the injected polyurethane, making it difficult to increase the rigidity of the reinforcing material and preventing excessive deformation of the deformable structure corresponding to the spokes.
- the problem that this invention aims to solve is to provide a manufacturing method and manufacturing device that can produce airless tires that suppress excessive deformation of the spokes.
- the present invention solves the above problem by applying a first force to a number of spokes toward the radial center of the wheel so that a first distance between the center of the wheel and the other end of each spoke that is joined to the wheel is reduced, and then arranging the tread and the wheel with the first force applied to the number of spokes so that the first inner circumferential surface faces the other end, and then removing the first force applied to the number of spokes.
- the present invention also solves the above problem by applying a third force in the radial direction of the inner ring and a fourth force in the opposite direction to the third force to the multiple spokes so that a second distance between the center of the inner ring and the other end of each spoke, one end of which is joined to the inner ring, is reduced; the tread and the inner ring with the third and fourth forces applied to the multiple spokes are positioned so that the other ends of the spokes face the first inner surface of the tread; and the third and fourth forces applied to the multiple spokes are removed.
- the present invention makes it possible to manufacture airless tires that suppress excessive deformation of the spokes.
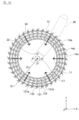
- FIG. 1 is a front view illustrating an example of an airless tire according to an embodiment of the present invention.
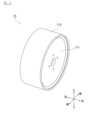
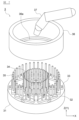
- FIG. 2 is a perspective view showing an example of the wheel shown in FIG. 1 .
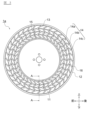
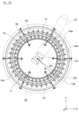
- FIG. 2 is a front view illustrating another example of an airless tire according to an embodiment of the present invention.
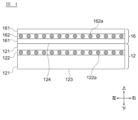
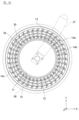
- FIG. 4 is a cross-sectional view of a main portion showing the outer ring and the tread taken along the line AA in FIG. 3.
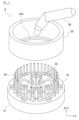
- FIG. 1 is a perspective view showing an example of an airless tire manufacturing apparatus according to an embodiment of the present invention.
- FIG. 6 is a plan view (part 1) showing a procedure for installing a wheel and a tread in the manufacturing apparatus shown in FIG. 5 .
- FIG. 1 is a front view illustrating an example of an airless tire according to an embodiment of the present invention.
- FIG. 2 is a perspective view showing an example of the wheel shown in FIG. 1 .
- FIG. 2 is a front view illustrating another example of an airless tire according to an embodiment of
- FIG. 6 is a plan view (part 2) showing the procedure for installing the wheel and the tread in the manufacturing apparatus shown in FIG. 5 .
- FIG. 6 is a plan view (part 3) showing the procedure for installing the wheel and the tread in the manufacturing apparatus shown in FIG. 5 .
- FIG. 2 is a perspective view showing another example of an airless tire manufacturing apparatus according to an embodiment of the present invention.
- FIG. 8 is a plan view (part 1) showing the procedure for handling the wheel, the tread, and the inner ring in the manufacturing apparatus shown in FIG. 7 .
- FIG. 8 is a plan view (part 2) showing the procedure for handling the wheel, the tread, and the inner ring in the manufacturing apparatus shown in FIG. 7 .
- FIG. 8 is a plan view (part 3) showing the procedure for handling the wheel, tread, and inner ring in the manufacturing apparatus shown in FIG. 7 .
- FIG. 2 is a front view illustrating an example of a spoke of the airless tire according to the embodiment of the present invention.
- FIG. 11 is a front view showing another example of a spoke of the airless tire according to the embodiment of the present invention.
- the side (outside) of a vehicle when an airless tire is mounted on the vehicle is defined as the front side.
- front rear
- upper lower
- lower right
- left respectively indicate the front, rear, upper, lower, right, and left of a vehicle on which an airless tire is mounted
- X-axis and Y-axis respectively indicate the horizontal and vertical directions when an airless tire manufacturing device (hereinafter also simply referred to as the manufacturing device) is viewed in a plane
- the Z-axis indicates the height direction relative to the installation position of the manufacturing device.
- the radial direction of the airless tire will be simply referred to as the radial direction
- the circumferential direction of the airless tire will be simply referred to as the circumferential direction.
- the radial direction of the airless tire is the same direction as the radial direction of the wheel and the inner ring
- the circumferential direction of the airless tire is the same direction as the circumferential direction of the wheel and the inner ring.
- FIG. 1 is a front view showing an example of an airless tire according to an embodiment of the present invention.
- An airless tire is a tire that supports a vehicle body by the reaction force of spokes made of an elastic material (hereinafter also referred to as an elastic material) rather than by air pressure.
- the airless tire of this embodiment can be applied to four-wheeled automobiles, two-wheeled automobiles, industrial vehicles, bicycles, and other vehicles, as well as carts.
- the airless tire 1 of this embodiment includes a wheel 11, a tread 12, spokes 13, and an intermediate ring 14.
- the wheel 11 is a member that is fixed to the vehicle hub (not shown) to connect with the vehicle, and is made of metal or other highly rigid materials. As shown in FIG. 2, the wheel 11 is made up of a disk 111 and a cylindrical rim 112. The disk 111 is shown in FIG. 1 as a circular member in the center of the airless tire 1, and the disk 111 is fixed to the vehicle hub to support the airless tire 1 on the axle. The shape of the wheel 11 can be set appropriately according to the required specifications of the airless tire 1.
- the disk 111 and the rim 112 may be molded as a single unit, or may be combined after being molded separately.
- the tread 12 is a cylindrical member having a tire width, and is disposed on the outermost periphery of the airless tire 1 to come into contact with the road surface.
- the tread 12 is made of a composite material in which an elastic material such as natural rubber or synthetic rubber is reinforced with metal or resin tire cords.
- a tread pattern is formed on the outer periphery of the tread 12, similar to that of conventional pneumatic tires, and forms the contact surface with the road surface.
- the inner diameter, outer diameter, thickness, and shape of the tread pattern of the tread 12 can be set as appropriate according to the required specifications of the airless tire 1.
- the spokes 13 are members that support the load (e.g., the vehicle weight) applied to the airless tire 1, and are plate-like members made of an elastic material such as elastic thermoplastic resin or elastic thermosetting resin, with a width equivalent to the tire width.
- the spokes 13 extend radially from the outer periphery of the wheel 11 (specifically, the outer periphery of the rim 112) toward the inner periphery of the tread 12, and are provided at equal intervals and spaced apart from each other along the circumferential direction of the airless tire 1.
- the spokes 13 are provided symmetrically with respect to the central axis of the airless tire 1. There is no particular limit to the number of spokes 13 provided on one airless tire 1, and can be set appropriately depending on the ground contact length of the airless tire 1, the load-bearing value of the spokes 13, vibration resistance, and other required specifications of the airless tire 1.
- the means for attaching the spokes 13 to the wheel 11 is not particularly limited as long as robustness can be ensured.
- a groove may be formed in the outer peripheral surface (hereinafter also referred to as the first outer peripheral surface) of the rim 112 that constitutes the wheel 11, and the inner peripheral end (hereinafter also referred to as the one end) of the spokes 13 may be fitted into this groove.
- the first outer peripheral surface and the one end may also be bonded with an adhesive, or may be connected with a bolt.
- the means for attaching the spokes 13 to the tread 12 is not particularly limited as long as robustness can be ensured.
- the inner peripheral surface (hereinafter also referred to as the first inner peripheral surface) of the tread 12 and the outer peripheral end (hereinafter also referred to as the other end) of the spokes 13 may be bonded with an adhesive, or may be connected with a bolt.
- the intermediate ring 14 is a member that transmits the deformation of the spokes 13 in the circumferential direction to the adjacent spokes 13 in order to support the load by the entire airless tire 1 when the spokes 13 are deformed by a radial load.
- the intermediate ring 14 is made of an elastic material such as an elastic thermoplastic resin or an elastic thermosetting resin, like the spokes 13.
- the intermediate ring 14 is formed in a cylindrical shape concentric with the wheel 11 and the tread 12, and is provided between the wheel 11 and the tread 12 to connect the multiple spokes 13 to each other.
- the means for attaching the intermediate ring 14 to the spokes 13 as long as robustness can be ensured.
- the intermediate ring 14 is bonded to the spokes 13 by an adhesive.
- the spokes 13 and the intermediate ring 14 may be integrally molded.
- the airless tire 1 shown in FIG. 1 has three intermediate rings 14a, 14b, and 14c, but the number of intermediate rings 14 provided in one airless tire 1 is not particularly limited.
- FIG. 3 is a front view showing another example of an airless tire according to an embodiment of the present invention.
- the airless tire 1a shown in FIG. 3 includes an inner ring 15 and an outer ring 16 in addition to a wheel 11, a tread 12, spokes 13, and an intermediate ring 14.
- the inner ring 15 is an annular member that connects one end of the multiple spokes 13, and is made of, for example, the same material as the spokes 13.
- the inner side of the inner ring 15 is bonded to the outer side of the wheel 11.
- a protrusion is provided on the inner surface of the inner ring 15 (hereinafter also referred to as the third inner surface) and the protrusion is fitted into a groove formed in the first outer surface to bond them.
- the third inner surface and the first outer surface may be bonded with an adhesive.
- the outer side of the inner ring 15 is also bonded to the spokes 13.
- one end of the spokes 13 is bonded to the outer surface of the inner ring 15 (hereinafter also referred to as the third outer surface) with an adhesive.
- the inner ring 15 may be molded integrally with the spokes 13.
- the outer ring 16 is an annular member that connects the other ends of the multiple spokes 13, and is made of, for example, the same material as the spokes 13.
- the outer side of the outer ring 16 is bonded to the inner side of the tread 12.
- the outer surface (hereinafter also referred to as the second outer surface) of the outer ring 16 and the first inner surface are bonded with an adhesive.
- the inner side of the outer ring 16 is bonded to the spokes 13.
- the other ends of the spokes 13 are bonded to the inner surface (hereinafter also referred to as the fourth inner surface) of the outer ring 16 with an adhesive.
- the outer ring 16 may be molded integrally with the spokes 13.
- the spokes 13, the inner ring 15, and the outer ring 16 may be molded integrally, or the spokes 13, the intermediate ring 14, the inner ring 15, and the outer ring 16 may be molded integrally.
- the contact area with the rim 112 is increased compared to when the spokes 13 are directly connected to the wheel 11, improving the load-bearing capacity of the airless tire 1a.
- the contact area with the tread 12 is increased compared to when the spokes 13 are directly connected to the tread 12, improving the load-bearing capacity of the airless tire 1a.
- the inner ring 15 and the outer ring 16 have a width equivalent to the tire width (for example, a width within a range of tire width ⁇ 5%) and an appropriate thickness according to the required specifications of the airless tire 1a.
- the spokes 13 extend radially from the third outer peripheral surface toward the first inner peripheral surface, connecting the inner ring 15 and the tread 12. If the airless tire has an outer peripheral ring 16, the spokes 13 extend radially from the first outer peripheral surface toward the fourth inner peripheral surface, connecting the wheel 11 and the outer peripheral ring 16. If the airless tire has an inner ring 15 and an outer peripheral ring 16 like the airless tire 1a shown in FIG. 3, the spokes 13 extend radially from the third outer peripheral surface toward the fourth inner peripheral surface, connecting the inner ring 15 and the outer peripheral ring 16.
- FIG. 4 is a cross-sectional view of the outer ring 16 and the tread 12 in the A-A cross section of FIG. 3, which is a cross section perpendicular to the circumferential direction of the airless tire 1a.
- the tread 12 shown in FIG. 4 is in contact with the road surface and has a first elastic portion 121 made of an elastic material and a first reinforcing layer 122 extending in the width direction of the tread 12 (left and right direction of the vehicle).
- the first reinforcing layer 122 includes tire cords 122a and hard rubber, and has a higher rigidity than the first elastic portion 121 made of an elastic material.
- the first reinforcing layer 122 is positioned closer to the first inner circumferential surface 124 than the contact surface 123 that is in contact with the road surface.
- the outer ring 16 shown in FIG. 4 has a second elastic portion 161 made of an elastic material, and a second reinforcing layer 162 extending in the width direction of the outer ring 16 (left and right direction of the vehicle).
- the second reinforcing layer 162 includes tire cords 162a and hard rubber, and has higher rigidity than the second elastic portion 161.
- the tread 12 of the airless tire 1 shown in FIG. 1 also has a first elastic portion 121 and a first reinforcing layer 122.
- intermediate ring 14, the inner ring 15, and the outer ring 16 are not essential components of the airless tire according to the embodiment of the present invention, and may be provided as needed or may be omitted.
- a wheel 11 and a tread 12 are prepared, and an airless tire is manufactured by combining the wheel 11 and the tread 12.
- the wheel 11 includes a plurality of spokes 13 that extend radially from a first outer peripheral surface to which one end is joined, and that are deformable in the radial direction, with the distance between the center of the wheel 11 and the other end being a predetermined distance longer than the radius of the first inner peripheral surface 124.
- the plurality of spokes 13 When combining the wheel 11 and the tread 12, the plurality of spokes 13 are deformed in the circumferential direction and/or radial direction so that the distance between the center of the wheel 11 and the other end is reduced (e.g., to be less than the radius of the first inner peripheral surface 124), and the tread 12 and the plurality of spokes 13 in the deformed state are arranged so that the first inner peripheral surface and the other end face each other, and the plurality of spokes 13 in the deformed state are returned to their pre-deformed state.
- Two embodiments of the manufacturing method of an airless tire are described below.
- FIG. 5 is a perspective view showing an example of a manufacturing apparatus according to an embodiment of the present invention.
- the manufacturing apparatus 2 shown in FIG. 5 is an apparatus for manufacturing an airless tire that does not have an inner ring 15 and in which the spokes 13 are directly joined to the wheel 11, like the airless tire 1 shown in FIG. 1.
- the manufacturing apparatus 2 includes a first base 21, a fixed member 22, a first movable member 23, a first pin 24, and conveying mechanisms 25 and 26.
- the first pedestal 21 is a member that supports the equipment that constitutes the manufacturing apparatus 2.
- the first pedestal 21 is installed, for example, on a level ground, and its position is fixed by anchor bolts or the like.
- the first pedestal 21 has an appropriate shape and rigidity within a range that allows it to adequately support the equipment that constitutes the manufacturing apparatus 2.
- the fixing member 22 is a member that fixes the wheel 11 to the first base 21, and is not particularly limited as long as it is capable of fixing the wheel 11 to the first base 21.
- the fixing member 22 shown in FIG. 5 has a base portion that is provided in the center of the first base 21 and is fixed to the first base 21 (or is part of the first base 21), and a pin that is inserted into a hole provided in the disc 111.
- the hole in the disc 111 is a hole through which a bolt is inserted when connecting the wheel 11 to the vehicle.
- the Z-axis direction is the width direction of the wheel 11.
- the first moving members 23 are members attached to the first base 21, and are movable in the radial direction of the wheel 11 fixed to the fixed member 22.
- six first moving members 23 are attached to the first base 21 shown in FIG. 5, and each of the six first moving members 23 moves independently in the radial direction on the XY plane perpendicular to the Z axis.
- the first moving members 23 include, for example, a worm gear (not shown) extending in the radial direction, and the first moving members 23 are moved in the radial direction by rotating this worm gear by a motor or the like.
- the first pin 24 is a pin fixed to the first moving member 23 along the circumferential direction, and as shown in FIG. 5, a plurality of first pins 24 are fixed to each first moving member 23. One end of the first pin 24 is fixed to the first moving member 23, and extends in the Z-axis direction (width direction of the wheel 11).
- the method of fixing the first pin 24 to the first moving member 23 is not particularly limited, and the first pin 24 may be fixed by a bolt or adhesive, or the first moving member 23 and the first pin 24 may be integrally molded.
- the first pin 24 is a pin that applies a first force to the spoke 13 in the radial direction (specifically, toward the center in the radial direction), and therefore has an appropriate shape and rigidity within a range in which the spoke 13 made of an elastic material can be deformed.
- the arrangement of the first pin 24 can be appropriately set within a range in which the spoke 13 can be appropriately deformed, and the shape of the first moving member 23 depends on the arrangement of the first pin 24. The first force will be described later.
- the transport mechanism 25 is a mechanism for transporting the tread 12, and is not particularly limited as long as it can properly position the tread 12 in the manufacturing apparatus 2.
- the transport mechanism 25 shown in FIG. 5 is a cylindrical member, and a support part 25a for supporting the tread 12 is provided at the lower end of the inner circumference side of the transport mechanism 25.
- the transport mechanism 25 is moved in the X-axis direction, the Y-axis direction, and the Z-axis direction by an arm (not shown) provided above the manufacturing apparatus 2, or the like.
- the transport mechanism 26 is a mechanism for transporting the wheel 11 and the inner ring 15, and removes the manufactured airless tire 1 from the manufacturing apparatus 2.
- the transport mechanism 26 is, for example, a robot arm as shown in FIG. 5, but is not particularly limited as long as it can properly handle the wheel 11, etc.
- step S1 When manufacturing the airless tire 1 shown in FIG. 1 using the manufacturing apparatus 2 shown in FIG. 5, first prepare the wheel 11 having a plurality of spokes 13 extending radially from a first outer peripheral surface to which one end is joined and deformable in the radial direction of the wheel 11, and the tread 12 (step S1).
- the wheel 11 having the spokes 13 is manufactured by integrally molding the spokes 13 and the intermediate ring 14 made of an elastic material (e.g., urethane resin such as thermoplastic polyurethane) using a molding method such as injection molding or vacuum casting, and joining one end of the spokes 13 to the first outer peripheral surface of the disk 111.
- an elastic material e.g., urethane resin such as thermoplastic polyurethane
- the method of joining the one end of the spokes 13 to the first outer peripheral surface is not particularly limited as long as robustness can be ensured.
- the wheel 11 may be inserted into a mold and integrally molded (insert molding) with the spokes 13 and the intermediate ring 14.
- the tread 12 is manufactured by, for example, wrapping the tire cord 122a corresponding to the first reinforcing layer 122 with raw rubber corresponding to the first elastic portion 121 to form a prepreg, and then heating and pressurizing the prepreg (vulcanizing it).
- the shapes of the spokes 13 and the intermediate ring 14 can be set appropriately within a range in which the spokes 13 can be deformed in the radial direction by the first pin 24.
- the diameter of the wheel 11 and the length of the spokes 13 are set so that the first distance from the center of the wheel 11 to the other ends of the multiple spokes 13 is a first predetermined distance longer than the radius of the first inner circumferential surface.
- the first distance D1 from the center C1 of the wheel to the other ends E1 of the spokes 13 is set to be a first predetermined distance longer than the radius B of the first inner circumferential surface 124 shown in FIG. 6B.
- the first predetermined distance can be set appropriately within a range in which the other ends E1 of the spokes 13 can be pressed against the first inner circumferential surface 124 and the spokes 13 can be fixed to the tread 12, and is, for example, 5 to 10% of the radius B of the first inner circumferential surface 124.
- the wheel 11 having a plurality of spokes 13 is transported by a transport mechanism 26 shown by dashed lines in Fig. 6A, and the pins of the fixing member 22 are inserted into the holes in the disk 111 to fix the wheel 11 to the fixing member 22 (step S2).
- the first pins 24 are disposed between adjacent spokes 13, so that when the wheel 11 is fixed to the fixing member 22, the first pins 24 are inserted between adjacent spokes 13 as shown in Fig. 6A.
- the number of first pins 24 does not necessarily need to be the same as the number of spokes 13, and for example, the first pins 24 may be disposed every other spoke 13 between adjacent spokes 13.
- a first radial force is applied to the multiple spokes 13 so that the first distance D1 shown in FIG. 6A is less than the radius B of the first inner circumferential surface 124 shown in FIG. 6B (step S3).
- the first moving member 23 is moved radially toward the center C1 (in the direction of the arrow shown in FIG. 6A), and a first force is applied to the multiple spokes 13 via the intermediate ring 14c in contact with the first pin 24 so that the first distance D1 is less than the radius B of the first inner circumferential surface 124 for all spokes 13.
- the first force is applied to the spokes 13 by applying a second radial force to the intermediate ring 14c.
- the spokes 13 are deformed and the radial length is shortened (diameter is reduced), and as shown in FIG. 6B, the first distance D1 is shorter than the radius B of the first inner circumferential surface 124.
- a pin is used to apply the first force, but the means for applying force to the spokes 13 is not limited to a pin.
- the spokes 13 may be held by a clamp or the like, and the clamp holding the spokes 13 may be moved in the radial direction.
- the radial length of the spokes 13 to which the first force is applied may be different for each spoke 13.
- the direction of the arrow shown in FIG. 6A is also referred to as the first direction.
- the spokes 13 may have multiple bends between one end and the other end that bend in the direction connecting the one end and the other end.
- the spokes 13 shown in FIG. 6A have bends 131, 132, and 133 between one end and the other end that deform in the circumferential direction.
- the intermediate ring 14 may also connect the bends of the spokes 13 to each other.
- the intermediate ring 14a shown in FIG. 6A connects the bend 131 to bends 131a and 131b of adjacent spokes 13.
- the diameter of the spokes 13 can be reduced with a smaller force.
- the airless tire 1 includes an intermediate ring 14, the circumferential and radial deformations of the spokes 13 are transmitted to adjacent spokes 13 by the intermediate ring 14. Therefore, when applying a second force to the intermediate ring 14 to make the first distance D1 less than the radius B of the first inner circumferential surface 124, the second force may be applied to only a portion of the intermediate ring 14. For example, every other first pin 24 shown in FIG. 5 is thinned out so that every other first pin 24 is disposed between adjacent spokes 13. This makes it possible to prevent the spokes 13 from being narrowed more than necessary.
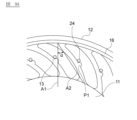
- FIG. 9A is a front view showing an example of a spoke 13 of an airless tire according to an embodiment of the present invention.
- the wheel 11 shown in FIG. 9A includes a plurality of spokes 13 and an outer circumferential ring 16, and the tread 12 is joined to the outer circumferential ring 16.
- the spoke 13 shown in FIG. 9A has a first protrusion P1, and the first pin 24 is in contact with the first protrusion P1. As shown in FIG.
- the radial direction A1 and the direction A2 connecting one end of the spoke 13 to the other end form a minor angle ⁇ within a predetermined range.
- the first force is applied to the first protrusion P1.
- the shape of the first protrusion P1 and the predetermined range of the minor angle ⁇ can be appropriately set within a range in which the first force can be appropriately applied to the first protrusion P1, and the predetermined range is, for example, 10 to 30°.
- the tread 12 is transported using the transport mechanism 25 shown by the dashed line in Fig. 6B, and the tread 12 and the wheel 11 with the first force applied to the spokes 13 are positioned so that the first inner circumferential surface 124 faces the other end E1 (step S4).
- the transport mechanism 25 with the tread 12 supported on the support portion 25a is moved from above to below the manufacturing device 2 along the Z-axis direction, and the tread 12 is positioned outside the spokes 13 with the first force applied so that the first inner circumferential surface 124 faces the other end E1.
- the transport mechanism 26 moves to a position that does not impede the movement of the transport mechanism 25.
- step S5 With the wheel 11 and tread 12 positioned such that the first inner circumferential surface 124 and the other end E1 face each other, the first force applied to the spokes 13 is removed, and the other end E1 of the spokes 13 is pressed against the first inner circumferential surface 124 to make intimate contact, and the spokes 13 are fixed to the tread 12 (step S5).
- the first moving member 23 is moved radially toward the first inner circumferential surface 124 (in the direction of the arrow shown in FIG. 6B), and the first force is removed from the spokes 13.
- the first distance D1 is longer than the radius B of the first inner circumferential surface 124, so that the other end E1 of the spokes 13 is pressed against the first inner circumferential surface 124 and fixed to the first inner circumferential surface 124.
- the other end E1 of the spoke 13 is pressed against the first inner circumferential surface 124, causing circumferential tensile stress in the tire cord 122a of the tread 12.
- the first direction of the arrow shown in FIG. 6A and the direction of the arrow shown in FIG. 6B are opposite to each other.
- step S6 The airless tire 1 manufactured by combining the wheel 11 and the tread 12 is removed from the manufacturing apparatus 2 using the conveying mechanism 26 (step S6).
- the removed airless tire 1 is conveyed to the next step.
- the conveying mechanism 26 then conveys a new wheel (step S7). Steps S2 to S7 are repeated until the desired number of airless tires 1 have been manufactured. Furthermore, if the wheel 11 and tread 12 are required, step S1 is executed as necessary.
- the wheel 11 may have, in addition to the multiple spokes 13, an outer ring 16 having a second outer surface with a second diameter that is longer than the first diameter of the first inner surface 124 by a first predetermined length.
- the first predetermined length can be set to an appropriate value within the range in which the second outer surface can be pressed against the first inner surface 124 and the outer ring 16 can be fixed to the tread 12, and is, for example, 2.5 to 5% of the first diameter of the first inner surface 124.
- the first predetermined length is also simply referred to as the predetermined length.
- step S3a the manufacturing device 2 applies a first force to the spokes 13 so that the maximum value of the diameter of the second outer surface is less than the first diameter. Then, the tread 12 and the wheel 11 with the first force applied to the spokes 13 are arranged so that the first inner surface 124 and the second outer surface face each other (step S4a), the first force applied to the spokes 13 is removed, and the second outer surface is pressed against the first inner surface 124 to be in close contact (step S5a).
- step S1 the wheel 11 including the spokes 13 and the outer ring 16 is prepared, and steps S3 to S5 are replaced by steps S3a to S5a.
- step S3a it is not necessary for the diameter of the second outer surface to be uniformly reduced, and it is sufficient that the maximum value of the diameter of the second outer surface is less than the first diameter.
- the wheel 11 having the spokes 13 and the outer ring 16 is fixed to the fixed member 22 by the transport mechanism 26, the first moving member 23 is moved in a first direction on the XY plane, and a second force is applied to the intermediate ring 14c in contact with the first pin 24 so that the maximum value of the diameter of the second outer peripheral surface is less than the first diameter.
- the transport mechanism 25 with the tread 12 supported on the support portion 25a is moved from above to below the manufacturing device 2 along the Z axis direction, and the tread 12 is positioned outside the multiple spokes 13 to which the first force is applied so that the first inner peripheral surface 124 and the second outer peripheral surface face each other, and the first moving member 23 is moved in a direction opposite to the first direction on the XY plane to remove the first force from the spokes 13.
- the manufacturing device 2 is used to replace the tread 12 of the airless tire 1 with another tread.
- the conveying mechanism 25 moved downward in the Z-axis direction as shown in FIG. 6B
- the wheel 11 of the airless tire 1 is fixed to the fixed member 22 by the conveying mechanism 26.
- the first moving member 23 is moved in the first direction to apply a second force to the intermediate ring 14c so that the first distance D1 is less than the radius B of the first inner circumferential surface 124, and the multiple spokes 13 fixed to the tread 12 are separated from the tread 12.
- the tread 12 separated from the multiple spokes 13 is conveyed to the next process (e.g., a regeneration process) by the conveying mechanism 25.
- a tread different from the separated tread 12 is placed on the support portion 25a of the transport mechanism 25, and the transport mechanism 25 is moved to place the other tread and the wheel 11 with the first force applied to the multiple spokes 13 (the second force applied to the intermediate ring 14c) so that the inner circumferential surface of the other tread (hereinafter also referred to as the second inner circumferential surface) faces the other end E1.
- the first moving member 23 is moved in the direction opposite to the first direction to remove the first force applied to the multiple spokes 13, and the multiple spokes 13 are fixed to the other tread.
- the airless tire 1 with the replaced tread 12 is removed from the manufacturing apparatus 2 by the transport mechanism 26.
- the wheel 11 When the wheel 11 has an outer ring 16 and the tread 12 of the airless tire 1 is replaced with another tread using the manufacturing device 2, the wheel 11 is fixed to the fixing member 22, and then the first moving member 23 is moved in the first direction to apply a second force to the intermediate ring 14c so that the maximum value of the diameter of the second outer peripheral surface is less than the first diameter, and the multiple spokes 13 fixed to the tread 12 are separated from the tread 12.
- Second Embodiment Fig. 7 is a perspective view showing another example of a manufacturing apparatus according to an embodiment of the present invention.
- the manufacturing apparatus 3 shown in Fig. 7 is an apparatus for manufacturing an airless tire having an inner circumferential ring 15 and in which the spokes 13 are not directly joined to the wheel 11, like the airless tire 1a shown in Fig. 3.
- the manufacturing apparatus 3 includes a second base 31, a second moving member 32, a third moving member 33, a second pin 34, a third pin 35, and transport mechanisms 36 and 37.
- the second base 31 is a member that supports the equipment that constitutes the manufacturing apparatus 3, and is fixed in position in the same manner as the first base 21.
- the second base 31 has an appropriate shape and rigidity within a range that allows it to adequately support the equipment that constitutes the manufacturing apparatus 3.
- the second moving member 32 and the third moving member 33 are members attached to the second base 31 and are movable in the radial direction relative to the second base 31.
- the second moving member 32 and the third moving member 33 shown in FIG. 7 move in the radial direction on the XY plane perpendicular to the Z axis.
- the mechanism by which the second moving member 32 and the third moving member 33 move is the same as that of the first moving member 23.
- the third moving member 33 is positioned outward of the second moving member 32.
- the second pin 34 is a pin fixed to the second moving member 32 along the circumferential direction, and as shown in FIG. 7, a plurality of second pins 34 are fixed to the second moving member 32. One end of the second pin 34 is fixed to the second moving member 32 and extends in the Z-axis direction. There is no particular limitation on the method of fixing the second pin 34.
- the second moving member 32 and the second pin 34 may be integrally molded.
- the third pin 35 is a pin fixed to the third moving member 33 along the circumferential direction, and as shown in FIG. 7, a plurality of third pins 35 are fixed to the third moving member 33. One end of the third pin 35 is fixed to the third moving member 33 and extends in the Z-axis direction. There is no particular limitation on the method of fixing the third pin 35.
- the third moving member 33 and the third pin 35 may be integrally molded.
- the second pin 34 and the third pin 35 are pins that apply the third and fourth radial forces to the spoke 13, respectively, and therefore have an appropriate shape and rigidity within a range in which the spoke 13, which is made of an elastic material, can be deformed.
- the arrangement of the second pin 34 and the third pin 35 can be appropriately set within a range in which the spoke 13 can be appropriately deformed, and the radial distance between the second pin 34 and the third pin 35 can be appropriately set within a range in which the spoke 13 can be appropriately deformed.
- the shapes of the second moving member 32 and the third moving member 33 depend on the arrangement of the second pin 34 and the third pin 35, respectively. The third force and the fourth force will be described later.
- the transport mechanism 36 is a mechanism for transporting the tread 12 and has a support portion 36a that supports the tread 12.
- the transport mechanism 37 is a mechanism for transporting the wheel 11 and the inner ring 15.
- step S11 When manufacturing an airless tire in which one ends of the multiple spokes 13 shown in FIG. 1 are connected by an inner ring 15 using the manufacturing device 3 shown in FIG. 7, first prepare the wheel 11, the tread 12, and the inner ring 15 having a third outer peripheral surface to which one ends of the multiple spokes 13 are connected (step S11).
- step S11 When the manufacturing device 3 is used to join the tread 12 and the inner ring 15, and the wheel 11 and the inner ring 15 are joined separately, the tread 12 and the inner ring 15 having a third outer peripheral surface are prepared in step S11.
- the inner ring 15 has multiple spokes 13 that extend radially from the third outer peripheral surface to which one ends are joined and are deformable in the radial direction of the inner ring 15.
- the diameter (inner diameter) of the inner ring 15 is set to be shorter than the diameter (outer diameter) of the wheel 11 by a second predetermined length.
- the second predetermined length can be set to an appropriate value within a range in which the third inner peripheral surface can be appropriately joined to the first outer peripheral surface, for example, 1 to 5% of the diameter of the wheel 11.
- the inner peripheral ring 15 is molded integrally with the spokes 13 and the intermediate ring 14, which are made of an elastic material, using a molding method such as injection molding or vacuum casting.
- the manufacturing method of the tread 12 is the same as in the first embodiment, so a description thereof will be omitted.
- the shapes of the spokes 13 and the intermediate ring 14 can be set appropriately within a range in which the spokes 13 can be deformed in the radial direction by the second pin 34 and the third pin 35.
- the outer diameter of the inner ring 15 (i.e., the diameter of the third outer surface) and the length of the spokes 13 are set so that the second distance from the center of the inner ring 15 to the other ends of the multiple spokes 13 is longer than the radius B of the first inner surface 124 by a second predetermined distance.
- the second distance D2 from the center C2 of the inner ring 15 to the other ends E2 of the spokes 13 is set to be longer than the radius B of the first inner surface 124 by a second predetermined distance as shown in FIG. 8B.
- the second predetermined distance can be set appropriately within a range in which the spokes 13 can be fixed to the tread 12, similar to the first predetermined distance, and is, for example, 5 to 10% of the radius B of the first inner surface 124.
- the inner ring 15 having a plurality of spokes 13 is transported by a transport mechanism 37 shown by a dashed line in FIG. 8A, and the second pin 34 and the third pin 35 are inserted between adjacent spokes 13 (step S12).
- the Z-axis direction is the width direction of the airless tire.
- the second pin 34 and the third pin 35 are arranged so as to be inserted between adjacent spokes 13. Note that the second pins 34 and the third pins 35 do not necessarily need to be arranged in the same number as the number of spokes 13, and for example, the second pins 34 and the third pins 35 may be arranged every other one between adjacent spokes 13.
- a third radial force and a fourth force in the opposite direction to the third force are applied to the multiple spokes 13 so that the second distance D2 shown in FIG. 8A is less than the radius B of the first inner surface 124 shown in FIG. 8B (step S13).
- the second moving member 32 is moved radially (in the direction of the arrow shown on the inner side of FIG. 8A) toward the outer periphery (other end E2), and the third force is applied to the spokes 13 via the intermediate ring 14a in contact with the second pin 34.
- the third force is applied to the spokes 13 by applying a fifth radial force to the intermediate ring 14a (first intermediate ring).
- the third moving member 33 is moved radially (in the direction of the arrow shown on the outer periphery of FIG. 8A) toward the center C2, and the fourth force is applied to the spokes 13 via the intermediate ring 14c in contact with the third pin 35.
- a sixth force in the opposite direction to the fifth force is applied to the intermediate ring 14c (second intermediate ring) that is closer to the other end E2 than the intermediate ring 14a (first intermediate ring), thereby applying a fourth force to the spoke 13.
- the spoke 13 is deformed and the radial length is shortened (diameter is reduced), and as shown in FIG. 8B, the second distance D2 becomes shorter than the radius B of the first inner circumferential surface 124.
- the third force is applied to the spokes 13 via the intermediate ring 14a, but the second pin 34 may be arranged inside the inner ring 15 (so that the second pin 34 and the third inner surface face each other) and the third force may be applied to the spokes 13 via the inner ring 15.
- a pin is used to apply the third and fourth forces, but the means for applying the forces to the spokes 13 is not limited to pins.
- the ends of the spokes 13 may be held by clamps or the like, and the clamps holding the ends of the spokes 13 may be moved so that they approach each other.
- the radial length of the spokes 13 to which the third and fourth forces are applied may be different for each spoke 13.
- the second pin 34 and the third pin 35 may move in opposite directions relative to each other to apply the third and fourth forces to one spoke 13, and one of the second pin 34 and the third pin 35 may move in the radial direction and the other may be stationary.
- the direction of the arrow shown on the inner circumference side of FIG. 8A is also referred to as the second direction, and the direction of the arrow shown on the outer circumference side of FIG. 8A is also referred to as the third direction.
- the spokes 13 may have multiple bent portions between one end and the other end that bend in the direction connecting the one end and the other end.
- the spokes 13 shown in FIG. 8A have three bent portions that deform in the circumferential direction between one end and the other end, similar to the spokes 13 shown in FIG. 6A.
- the intermediate ring 14 may also connect the bent portions of the spokes 13 to each other.
- the intermediate ring 14a shown in FIG. 8A connects the bent portions of adjacent spokes 13 to each other, similar to the intermediate ring 14a shown in FIG. 6A.
- FIG. 8A by applying a third force and a fourth force to the intermediate ring 14 that connects the bent portions of the spokes 13 to each other, the diameter of the spokes 13 can be reduced with a smaller force.
- the airless tire includes an intermediate ring 14, the circumferential and radial deformations of the spokes 13 are transmitted to adjacent spokes 13 by the intermediate ring 14, and therefore when the third and fourth forces are applied to the intermediate ring 14 to make the second distance D2 less than the radius B of the first inner circumferential surface 124, the third and fourth forces may be applied only to a portion of the intermediate ring 14. For example, every other second pin 34 and third pin 35 shown in FIG. 7 are thinned out so that the second pin 34 and third pin 35 are arranged every other one between adjacent spokes 13. This makes it possible to prevent the spokes 13 from being narrowed more than necessary.
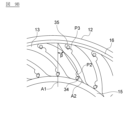
- Fig. 9B is a front view showing another example of the spoke 13 of the airless tire according to the embodiment of the present invention.
- the inner ring 15 shown in Fig. 9B has a plurality of spokes 13 and an outer ring 16, and the tread 12 is joined to the outer ring 16.
- the radial direction A1 and the direction A2 connecting one end of the spoke 13 to the other end form a minor angle ⁇ within a predetermined range.
- the third force is applied to the second protrusion P2, and the fourth force is applied to the third protrusion P3.
- the shapes of the second protrusion P2 and the third protrusion P3 and the specified range of the minor angle ⁇ can be set appropriately within a range in which the third force and the fourth force can be appropriately applied to the second protrusion P2 and the third protrusion P3, respectively, and the specified range is, for example, 10 to 30°.
- step S14-1 the tread 12 is transported using the transport mechanism 36 shown by the dashed lines, and the tread 12 and the inner ring 15 with the third and fourth forces applied to the spokes 13 are arranged so that the first inner surface 124 faces the other end E2 (step S14-1). Furthermore, the wheel 11 is transported using the transport mechanism 37 shown by the dashed lines in FIG. 8B, and the wheel 11 and the inner ring 15 with the third and fourth forces applied to the spokes 13 are arranged so that the first outer surface of the wheel 11 faces the third inner surface of the inner ring 15 (step S14-2). If the tread 12 and the inner ring 15 are joined using the manufacturing device 3 and the wheel 11 and the inner ring 15 are joined separately, step S14-2 is not performed and the wheel 11 is not arranged.
- the conveying mechanism 36 with the tread 12 supported on the support portion 36a is moved from above to below the manufacturing device 3 along the Z-axis direction, and the tread 12 is arranged on the outside of the spokes 13 so that the first inner circumferential surface 124 faces the other end E2.
- the wheel 11 is gripped by the conveying mechanism 37, and the wheel 11 is arranged on the inside of the inner ring 15 so that the first outer circumferential surface faces the third inner circumferential surface.
- the manufacturing device 3 may have a fixing member for fixing the wheel 11, as in the manufacturing device 2, and the wheel 11 gripped by the conveying mechanism 37 may be fixed to the second pedestal 31 by the fixing member.
- step S15 With the wheel 11, tread 12 and inner ring 15 positioned so that the first outer surface faces the third inner surface and the other end E2 faces the first inner surface 124, the third and fourth forces applied to the spokes 13 are removed and the other ends E2 of the spokes 13 are pressed against the first inner surface 124 to adhere to it, and the spokes 13 are fixed to the tread 12 (step S15). If the tread 12 and inner ring 15 are joined using the manufacturing device 3 and the wheel 11 and inner ring 15 are joined separately, in step S15, with the tread 12 and inner ring 15 positioned so that the other ends E2 faces the first inner surface 124, the third and fourth forces applied to the spokes 13 are removed.
- the second moving member 32 is moved radially toward the center C2 (in the direction of the arrow shown on the inner peripheral side of Fig. 8B) to remove the third force from the spokes 13, and the third moving member 33 is moved radially toward the outer peripheral side (the other end E2) (in the direction of the arrow shown on the outer peripheral side of Fig. 8B) to remove the fourth force from the spokes 13.
- the second moving member 32 is moved radially toward the center C2 (in the direction of the arrow shown on the inner peripheral side of Fig. 8B) to remove the third force from the spokes 13
- the third moving member 33 is moved radially toward the outer peripheral side (the other end E2) (in the direction of the arrow shown on the outer peripheral side of Fig. 8B) to remove the fourth force from the spokes 13.
- the second moving member 32 is moved radially toward the center C2 (in the direction of the arrow shown on the inner peripheral side of Fig. 8B) to remove the third force from the spokes 13
- the second distance D2 is longer than the radius B of the first inner peripheral surface 124, so that the other end E2 of the spoke 13 is pressed against the first inner peripheral surface 124 and fixed to the first inner peripheral surface 124.
- the other end E2 of the spoke 13 is pressed against the first inner circumferential surface 124, generating circumferential tensile stress in the tire cord 122a of the tread 12.
- step S16 The airless tire manufactured by combining the wheel 11, tread 12, and inner ring 15 is removed from the manufacturing apparatus 3 using the transport mechanism 37 (step S16). If only the tread 12 and inner ring 15 are combined, the combined parts are removed from the manufacturing apparatus 3 using the transport mechanism 36. The removed airless tire is transported to the next process. The transport mechanism 37 then transports a new inner ring 15 (step S17). Steps S12 to S17 are repeated until the desired number of airless tires have been manufactured. Furthermore, if the wheel 11, tread 12, and inner ring 15 are required, step S11 is executed as necessary.
- the inner ring 15 may include an outer ring 16 having a second outer peripheral surface with a second diameter that is longer than the first diameter of the first inner peripheral surface 124 by a first predetermined length.
- the manufacturing device 3 applies a third force and a fourth force to the multiple spokes 13 so that the maximum value of the diameter of the second outer peripheral surface is less than the first diameter (step S13a).
- step S14-1a the tread 12 and the inner ring 15 with the third force and the fourth force applied to the multiple spokes 13 are arranged so that the first inner peripheral surface 124 and the second outer peripheral surface face each other
- step S14-2a the wheel 11 and the inner ring 15 with the third force and the fourth force applied to the multiple spokes 13 are arranged so that the first outer peripheral surface and the third inner peripheral surface face each other
- step S15a the third and fourth forces applied to the spokes 13 are removed, and the second outer peripheral surface is pressed against the first inner peripheral surface 124 to make it adhere closely.
- step S11 if the inner peripheral ring 15 includes the outer peripheral ring 16, in step S11, the inner peripheral ring 15 including the spokes 13 and the outer peripheral ring 16 is prepared, and steps S13 to S15 are replaced with steps S13a to S15a.
- step S13a it is not necessary for the diameter of the second outer peripheral surface to be uniformly reduced, and it is sufficient that the maximum value of the diameter of the second outer peripheral surface is less than the first diameter.
- step S14-2a is not performed and the wheel 11 is not placed.
- the conveying mechanism 37 is used to convey the spokes 13 and the inner ring 15 including the outer ring 16, and the second pin 34 and the third pin 35 are inserted between the adjacent spokes 13.
- the second moving member 32 is moved in the second direction on the XY plane
- the third moving member 33 is moved in the third direction on the XY plane, and a fifth force is applied to the intermediate ring 14a in contact with the second pin 34, and a sixth force is applied to the intermediate ring 14c in contact with the third pin 35, so that the maximum value of the diameter of the second outer peripheral surface is less than the first diameter.
- the manufacturing device 3 is used to replace the tread 12 of the airless tire with another tread.
- the conveying mechanism 36 moved downward in the Z-axis direction as shown in FIG. 8B
- the wheel 11 of the airless tire is placed at the center of the conveying mechanism 36 by the conveying mechanism 37.
- the third moving member 33 is moved in the third direction to apply a third force and a fourth force to the multiple spokes 13 fixed to the tread 12 so that the second distance D2 is less than the radius B of the first inner circumferential surface 124, and the multiple spokes 13 are separated from the tread 12.
- a tread different from the separated tread 12 is placed on the support portion 25a of the transport mechanism 36, and the transport mechanisms 36, 37 are moved to place the other tread and the inner ring 15 with the third and fourth forces applied to the multiple spokes 13 so that the second inner surface faces the other end E2. Then, the third moving member 33 is moved in the second direction to remove the third and fourth forces applied to the multiple spokes 13, and the multiple spokes 13 are fixed to the other tread.
- the airless tire with the replaced tread 12 is removed from the manufacturing device 3 by the transport mechanism 37.
- the inner ring 15 includes the outer ring 16
- the tread 12 of the airless tire 1 is replaced with another tread using the manufacturing device 2
- the inner ring 15 is inserted through the second pin 34 and the third pin 35, and then the second moving member 32 is moved in the second direction to apply a third force to the intermediate ring 14a and the third moving member 33 is moved in the third direction to apply a fourth force to the intermediate ring 14c so that the maximum value of the diameter of the second outer peripheral surface is less than the first diameter, and the multiple spokes 13 fixed to the tread 12 are separated from the tread 12.
- a wheel 11 having a first outer circumferential surface and coupled to a vehicle, and a tread 12 having a first inner circumferential surface 124 and contacting a road surface are prepared, and the wheel 11 includes a plurality of spokes 13 having one end which is an end on the inner circumferential side and the other end which is an end on the outer circumferential side.
- a first distance D1 from a center C1 of the wheel 11 to the other ends E1 of the spokes 13 is longer than a radius B of the first inner circumferential surface 124 by a first predetermined distance, a first force is applied to the spokes 13 toward the center in the radial direction so that the first distance D1 is reduced, the tread 12 and the wheel 11 in a state in which the first force is applied to the spokes 13 are arranged such that the first inner circumferential surface 124 and the other ends E2 face each other, and the first force applied to the spokes 13 is removed.
- the wheel 11 is prepared, which includes the plurality of spokes 13 and an outer peripheral ring 16 that has a second outer peripheral surface with a second diameter that is a predetermined length longer than the first diameter of the first inner peripheral surface 124 and connects the other end E1, and the first force is applied to the plurality of spokes 13 so that the maximum value of the diameter of the second outer peripheral surface is less than the first diameter, and the tread 12 and the wheel 11 with the first force applied to the plurality of spokes 13 are arranged so that the first inner peripheral surface 124 and the second outer peripheral surface face each other.
- This increases the bonding area with the tread 12, improving the load-bearing capacity of the airless tire.
- the first force is applied to the multiple spokes 13 fixed to the tread 12 so that the first distance D1 is less than the radius B, and the multiple spokes 13 are separated from the tread 12, and another tread different from the tread 12 and the wheel 11 with the first force applied to the multiple spokes 13 are arranged so that the second inner circumferential surface of the other tread faces the other end E1, and the first force applied to the multiple spokes 13 is removed to fix the multiple spokes 13 to the other tread.
- the spoke 13 has a first protrusion P1, and the direction A1 connecting the one end and the other end E1 of the spoke 13 forms a minor angle within a predetermined range with the radial direction A2, and when the first force is applied to the spoke 13, the first force is applied to the first protrusion P1. This makes it possible to apply the first force to the spoke 13 without providing an intermediate ring 14.
- the spokes 13 have multiple bends between the one end and the other end E1, and the bends are bent in the direction connecting the one end and the other end E1
- the airless tire includes an intermediate ring 14 that connects the bends of adjacent spokes, and the first force is applied to the spokes 13 by applying the second radial force to the intermediate ring 14. This makes it possible to reduce the first force required to deform the spokes 13.
- a first base 21 having a fixed position, a fixed member 22 provided on the first base 21 and fixing the wheel 11 to the first base 21, a first movable member 23 attached to the first base 21 so as to be movable in the radial direction, a plurality of first pins 24 extending in the width direction of the wheel 11 and fixed to the first movable member 23 along the circumferential direction of the wheel 11, the tread 12, and a device for transporting the tread 12 when positioning the wheel 11 in a state in which the first force is applied to the plurality of spokes 13 are arranged.
- the manufacturing device 2 includes conveying mechanisms 25 and 26 for conveying the wheel 11 to the fixed member 22, the first pin 24 is inserted between the adjacent spokes 13, the first moving member 23 is moved in a first direction to apply the first force to the multiple spokes 13 so that the first distance D1 is less than the radius B, the tread 12 is positioned outside the multiple spokes 13 to which the first force is applied so that the first inner circumferential surface 124 faces the other end E1, and the first moving member 23 is moved in a direction opposite to the first direction to remove the first force.
- a tread 12 having a first inner circumferential surface 124 and contacting the road surface, and an inner circumferential ring 15 having a third outer circumferential surface to which one end of the inner circumferential side of a plurality of spokes 13 is connected are prepared, the inner circumferential ring 15 has a plurality of spokes 13 that extend radially from the third outer circumferential surface to which the one end is joined and that are deformable in the radial direction of the inner circumferential ring 15, and a second distance D2 from a center C2 of the inner circumferential ring 15 to the other end E2 of the outer circumferential side of the plurality of spokes 13 is determined by the distance D2 from the first inner circumferential surface 124 to the other end E2 of the outer circumferential side of the plurality of spokes 13.
- a method for manufacturing an airless tire which applies a third radial force and a fourth force in a direction opposite to the third force to the spokes 13 so that the second distance D2 is reduced by a second predetermined distance longer than the radius B of the circumferential surface 124, and arranges the tread 12 and the inner ring 15 with the third and fourth forces applied to the spokes 13 so that the other end E2 faces the first inner circumferential surface 124, and removes the third and fourth forces applied to the spokes 13. This makes it possible to manufacture an airless tire that suppresses excessive deformation of the spokes 13.
- the third force and the fourth force are applied to the multiple spokes 13 fixed to the tread 12 so that the second distance D2 is less than the radius B, and the multiple spokes 13 are separated from the tread 12, and another tread different from the tread 12 and the inner ring 15 in a state in which the third force and the fourth force are applied to the multiple spokes 13 are arranged so that the second inner surface of the other tread faces the other end E2, and the third force and the fourth force applied to the multiple spokes 13 are removed to fix the multiple spokes 13 to the other tread.
- the spoke 13 has a second protrusion P2 and a third protrusion P3 located closer to the other end E2 than the second protrusion P2, and the direction A2 connecting the one end and the other end E2 of the spoke 13 forms a minor angle with the radial direction A1 within a predetermined range, and the third force is applied to the second protrusion P2 and the fourth force is applied to the third protrusion P3.
- the spokes 13 have multiple bends between the one end and the other end E2, and the bends are bent in the direction connecting the one end and the other end E2, and the airless tire includes multiple intermediate rings 14 that connect the bends of adjacent spokes 13, and applies the fifth force in the radial direction to a first intermediate ring and applies a sixth force in the opposite direction to the fifth force to a second intermediate ring that is closer to the other end than the first intermediate ring, thereby applying the third force and the fourth force to the multiple spokes 13. This makes it possible to reduce the first force required to deform the spokes 13.
- a manufacturing device 3 that includes a second base 31 whose position is fixed, a second movable member 32 that is attached so as to be movable in the radial direction relative to the second base 31, a third movable member 33 that is attached so as to be movable in the radial direction relative to the second base 31 and that is disposed outside the second movable member 32, a plurality of second pins 34 that extend in the width direction of the inner ring 15 and are fixed to the second movable member 32 along the circumferential direction of the inner ring 15, a plurality of third pins 35 that extend in the width direction of the inner ring 15 and are fixed to the third movable member 33 along the circumferential direction, a wheel 11 that is connected to a vehicle, the tread 12, and transport mechanisms 36, 37 that transport the wheel 11 and the tread 12 when arranging the inner ring 15 in a state in which the third force and the fourth force are applied to the plurality of spokes 13, and the manufacturing device
- the second pin 34 and the third pin 35 are inserted between the spokes 13, and the second moving member 32 is moved in the second direction to apply the third force to the plurality of spokes 13 and the third moving member 33 is moved in a third direction opposite to the second direction to apply the fourth force to the plurality of spokes 13 so that the second distance D2 is less than the radius B.
- the wheel 11 is disposed inside the inner ring 15 in a state in which the third force and the fourth force are applied to the plurality of spokes 13 so that the first outer surface of the wheel 11 and the third inner surface of the inner ring 15 face each other, and the tread 12 is disposed outside the plurality of spokes 13 in a state in which the third force and the fourth force are applied so that the other end E2 and the first inner surface 124 face each other, and the second moving member 32 is moved in the third direction and the third moving member 33 is moved in the second direction to remove the third force and the fourth force.
- This makes it possible to manufacture an airless tire that suppresses excessive deformation of the spokes 13.
- the tread 12 has a first elastic portion 121 made of an elastic material, and a first reinforcing layer 122 that extends in the width direction of the tread 12 and has a higher rigidity than the first elastic portion 121, and the first reinforcing layer 122 is disposed at a position closer to the first inner circumferential surface 124 than a contact surface 123 that contacts the road surface. This makes it possible to further suppress excessive deformation of the spokes 13.
- the outer ring 16 has a second elastic portion 161 made of an elastic material, and a second reinforcing layer 162 that extends in the width direction of the outer ring 16 and has a higher rigidity than the second elastic portion 161. This makes it possible to further suppress excessive deformation of the spokes 13.
- an airless tire manufacturing device having a plurality of spokes 13, each having one end which is an inner circumferential end and the other end which is an outer circumferential end, extending radially from a first outer circumferential surface of a wheel 11 which is connected to a vehicle toward a first inner circumferential surface 124 of a tread 12 which comes into contact with a road surface and which is deformable in the radial direction of the wheel 11, with the one ends of the plurality of spokes 13 being joined to the first outer circumferential surface
- the device comprising: a first base 21 having a fixed position; a fixing member 22 provided on the first base 21 and fixing the wheel 11 to the first base 21; a first movable member 23 attached to the first base 21 so as to be movable in the radial direction relative to the first base 21; a plurality of first pins 24 extending in the width direction of the wheel 11 and fixed to the first movable member 23 along the circumferential direction of the wheel 11; the tread 12
- the device includes a conveying mechanism 25, 26 for conveying the tread 12 when the wheel 11 is to be fixed to the fixed member 22, the first pin 24 is inserted between adjacent spokes 13 among the plurality of spokes 13, the first moving member 23 is moved in a first direction to apply a first force toward the center in the radial direction to the plurality of spokes 13 so that a first distance between the center of the wheel 11 to which the one end E1 is joined and the other ends of the plurality of spokes 13, which is longer than the radius B of the first inner circumferential surface 124 by a first predetermined distance, is reduced, the tread 12 and the wheel 11 in a state in which the first force is applied to the plurality of spokes 13 are arranged so that the first inner circumferential surface 124 and the other ends E1 face each other, and the first moving member 23 is moved in a direction opposite to the first direction to remove the first force.
- This makes it possible to manufacture an airless tire that suppresses excessive deformation of the spokes 13.
- an airless tire manufacturing device includes an inner ring 15 that connects one end, which is the inner end portion, of a plurality of spokes 13, and a plurality of spokes 13 that extend radially from a third outer peripheral surface of the inner ring 15 toward a first inner peripheral surface 124 of a tread 12 that comes into contact with a road surface and that are deformable in a radial direction of the inner ring 15, the device including a second base 31 whose position is fixed, a second movable member 32 that is attached to the second base 31 so as to be movable in the radial direction, and a second movable member 32 that is attached to the second base 31 so as to be movable in the radial direction.
- a third moving member 33 arranged outside the second moving member 32, a plurality of second pins 34 extending in the width direction of the inner ring 15 and fixed to the second moving member 32 along the circumferential direction of the inner ring 15, a plurality of third pins 35 extending in the width direction and fixed to the third moving member 33 along the circumferential direction of the inner ring 15, and transport mechanisms 36, 37 for transporting the tread 12 and the inner ring 15 when the tread 12 and the inner ring 15 are arranged,
- the second pin 34 is inserted between adjacent spokes 13 among the spokes 13, or the second pin 34 is disposed inside the inner circumferential ring 15, and the third pin 35 is inserted between adjacent spokes 13.
- the second moving member 32 is moved in a second direction to apply the third radial force to the plurality of spokes 13 so that a second distance D2, which is longer than the radius B of the first inner circumferential surface 124 by a second predetermined distance, between a center C2 of the inner circumferential ring 15 to which the one end is joined and the other end, which is the outer circumferential end of the plurality of spokes 13, is reduced.
- the third moving member 33 is moved in a third direction opposite to the second direction to apply a fourth force to the plurality of spokes 13 in the opposite direction to the third force, the tread 12 and the inner ring 15 in a state in which the third force and the fourth force are applied to the plurality of spokes 13 are disposed so that the other end E2 faces the first inner surface 124, and the second moving member 32 is moved in the third direction and the third moving member 33 is moved in the second direction to remove the third force and the fourth force.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Tires In General (AREA)
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2025552486A JPWO2025083751A1 (cg-RX-API-DMAC7.html) | 2023-10-16 | 2023-10-16 | |
| PCT/JP2023/037369 WO2025083751A1 (ja) | 2023-10-16 | 2023-10-16 | エアレスタイヤの製造方法及び製造装置 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/JP2023/037369 WO2025083751A1 (ja) | 2023-10-16 | 2023-10-16 | エアレスタイヤの製造方法及び製造装置 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2025083751A1 true WO2025083751A1 (ja) | 2025-04-24 |
Family
ID=95447994
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2023/037369 Ceased WO2025083751A1 (ja) | 2023-10-16 | 2023-10-16 | エアレスタイヤの製造方法及び製造装置 |
Country Status (2)
| Country | Link |
|---|---|
| JP (1) | JPWO2025083751A1 (cg-RX-API-DMAC7.html) |
| WO (1) | WO2025083751A1 (cg-RX-API-DMAC7.html) |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2017116385A1 (en) * | 2015-12-28 | 2017-07-06 | Compagnie Generale Des Etablissements Michelin | Method of forming non-pneumatic tire including pressure application between an intermediate section and an outer shear band ring |
| WO2018125195A1 (en) * | 2016-12-30 | 2018-07-05 | Compagnie Generale Des Etablissements Michelin | Fixture for spoke to shear band attachment for a non-pneumatic tire with spoke pre-compression |
| US20190184658A1 (en) * | 2017-12-18 | 2019-06-20 | The Goodyear Tire & Rubber Company | Nonpneumatic tire assembly method and apparatus |
| WO2020139680A1 (en) * | 2018-12-28 | 2020-07-02 | Bridgestone Americas Tire Operations, Llc | Web structure for non-pneumatic tire and method of making same |
| JP2022034664A (ja) * | 2020-08-19 | 2022-03-04 | 住友ゴム工業株式会社 | エアレスタイヤの製造方法 |
-
2023
- 2023-10-16 WO PCT/JP2023/037369 patent/WO2025083751A1/ja not_active Ceased
- 2023-10-16 JP JP2025552486A patent/JPWO2025083751A1/ja active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2017116385A1 (en) * | 2015-12-28 | 2017-07-06 | Compagnie Generale Des Etablissements Michelin | Method of forming non-pneumatic tire including pressure application between an intermediate section and an outer shear band ring |
| WO2018125195A1 (en) * | 2016-12-30 | 2018-07-05 | Compagnie Generale Des Etablissements Michelin | Fixture for spoke to shear band attachment for a non-pneumatic tire with spoke pre-compression |
| US20190184658A1 (en) * | 2017-12-18 | 2019-06-20 | The Goodyear Tire & Rubber Company | Nonpneumatic tire assembly method and apparatus |
| WO2020139680A1 (en) * | 2018-12-28 | 2020-07-02 | Bridgestone Americas Tire Operations, Llc | Web structure for non-pneumatic tire and method of making same |
| JP2022034664A (ja) * | 2020-08-19 | 2022-03-04 | 住友ゴム工業株式会社 | エアレスタイヤの製造方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| JPWO2025083751A1 (cg-RX-API-DMAC7.html) | 2025-04-24 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2141030B1 (en) | Non-pneumatic tire and method of manufacturing same | |
| US20190047328A1 (en) | Method of forming non-pneumatic tire using support structure deformation | |
| EP3397465B1 (en) | Method of forming non-pneumatic tire including pressure application between an intermediate section and an outer shear band ring | |
| CN109795145A (zh) | 无气式轮胎制造方法 | |
| EP3290230B1 (en) | Tire | |
| CN115916549B (zh) | 包括非充气轮胎的车轮 | |
| CN101309805A (zh) | 挠性非充气轮胎 | |
| EP3902690B1 (en) | Non-pneumatic tire having reinforced support structure | |
| JP7248540B2 (ja) | 非空気圧タイヤの製造方法 | |
| JP5084637B2 (ja) | 非空気圧タイヤの成形型、および非空気圧タイヤの製造方法 | |
| JP7790071B2 (ja) | エアレスタイヤ及びその製造方法 | |
| JP2025040722A (ja) | エアレスタイヤの製造方法及び製造装置 | |
| JP7859234B2 (ja) | エアレスタイヤ及びその製造方法 | |
| JP2025533064A (ja) | 非空気圧タイヤのスポーク構成要素のための撓み部材 | |
| JP7859233B2 (ja) | エアレスタイヤ及びその製造方法 | |
| JP7497646B2 (ja) | エアレスタイヤの製造方法 | |
| JP7552140B2 (ja) | エアレスタイヤ | |
| CN113939411A (zh) | 轮胎 | |
| JPH10211807A (ja) | 空気入りタイヤの中子 | |
| JP7790072B2 (ja) | エアレスタイヤ及びその製造方法 | |
| WO2005014310A1 (ja) | 空気入りランフラットタイヤ用の支持体の製造方法 | |
| JP7563093B2 (ja) | エアレスタイヤ及びエアレスタイヤの製造方法 | |
| RU2457949C1 (ru) | Способ и устройство для сборки шин для колес транспортного средства | |
| US20250319723A1 (en) | Non-Pneumatic Tire | |
| JP2010158920A (ja) | チューブ体、チューブ体の製造方法、及びタイヤ |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 23956005 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2025552486 Country of ref document: JP Kind code of ref document: A |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2025552486 Country of ref document: JP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |