WO2025005170A1 - 方向性電磁鋼板 - Google Patents
方向性電磁鋼板 Download PDFInfo
- Publication number
- WO2025005170A1 WO2025005170A1 PCT/JP2024/023292 JP2024023292W WO2025005170A1 WO 2025005170 A1 WO2025005170 A1 WO 2025005170A1 JP 2024023292 W JP2024023292 W JP 2024023292W WO 2025005170 A1 WO2025005170 A1 WO 2025005170A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- steel sheet
- grain
- annealing
- content
- heating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/26—Methods of annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/34—Methods of heating
- C21D1/40—Direct resistance heating
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D3/00—Diffusion processes for extraction of non-metals; Furnaces therefor
- C21D3/02—Extraction of non-metals
- C21D3/04—Decarburising
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/008—Heat treatment of ferrous alloys containing Si
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1244—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment
- C21D8/1255—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment with diffusion of elements, e.g. decarburising, nitriding
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1244—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment
- C21D8/1272—Final recrystallisation annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1294—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties involving a localised treatment
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/002—Ferrous alloys, e.g. steel alloys containing In, Mg, or other elements not provided for in one single group C22C38/001 - C22C38/60
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/004—Very low carbon steels, i.e. having a carbon content of less than 0,01%
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/008—Ferrous alloys, e.g. steel alloys containing tin
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/06—Ferrous alloys, e.g. steel alloys containing aluminium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/08—Ferrous alloys, e.g. steel alloys containing nickel
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/12—Ferrous alloys, e.g. steel alloys containing tungsten, tantalum, molybdenum, vanadium, or niobium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/14—Ferrous alloys, e.g. steel alloys containing titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/16—Ferrous alloys, e.g. steel alloys containing copper
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/34—Ferrous alloys, e.g. steel alloys containing chromium with more than 1.5% by weight of silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/60—Ferrous alloys, e.g. steel alloys containing lead, selenium, tellurium, or antimony, or more than 0.04% by weight of sulfur
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/14766—Fe-Si based alloys
- H01F1/14775—Fe-Si based alloys in the form of sheets
- H01F1/14783—Fe-Si based alloys in the form of sheets with insulating coating
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/14766—Fe-Si based alloys
- H01F1/14791—Fe-Si-Al based alloys, e.g. Sendust
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/16—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of sheets
- H01F1/18—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of sheets with insulating coating
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2201/00—Treatment for obtaining particular effects
- C21D2201/05—Grain orientation
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2221/00—Treating localised areas of an article
Definitions
- the present invention relates to a grain-oriented electrical steel sheet. This application claims priority based on Japanese Patent Application No. 2023-106861, filed on June 29, 2023, the contents of which are incorporated herein by reference.
- Grain-oriented electrical steel sheet contains silicon, and the crystal orientation of its crystal grains is concentrated near the Goss orientation (cubic ⁇ 110 ⁇ 001>), with the ⁇ 001> orientation, which is the axis of easy magnetization, being nearly aligned with the rolling direction in the steel sheet manufacturing process.
- Such grain-oriented electrical steel sheet is extremely useful as a material for the iron cores of transformers, etc.
- Important magnetic properties of grain-oriented electrical steel sheet include magnetic flux density, core loss, and noise characteristics.
- Magnetic flux density B8 is generally used as an index of magnetic flux density.
- Magnetic flux density B8 is the value of the magnetic flux density of a magnetized grain-oriented electrical steel sheet when a magnetizing force of 800 A/m is applied in the rolling direction.
- a grain-oriented electrical steel sheet with a higher magnetic flux density B8 value is more easily magnetized with a certain magnetizing force and has a higher magnetic flux density, making it suitable for small, highly efficient transformers.
- the iron loss W17/ 50 is generally used as an index of iron loss.
- the iron loss W17 /50 is the iron loss when a grain-oriented electrical steel sheet is excited with an AC current under conditions of a maximum magnetic flux density of 1.7 T and a frequency of 50 Hz. It can be said that the smaller the value of the iron loss W17/ 50 of a grain-oriented electrical steel sheet, the lower the energy loss and the more suitable it is for a transformer.
- the magnetostrictive velocity level (Lva) is also used as an index of noise characteristics.
- the magnetostrictive velocity level (Lva) is a value obtained by time-differentiating the magnetostrictive waveform during AC excitation, converting it to velocity, and applying A-weighting audibility correction, which is the frequency characteristic of human hearing.
- A-weighting audibility correction which is the frequency characteristic of human hearing.
- the characteristics of sound that humans can perceive are not necessarily constant at all frequencies, and can be expressed by an audible characteristic called A-weighting.
- the actual magnetostrictive waveform is not a sine wave, but a waveform in which various frequency components overlap.
- Patent Documents 1 and 2 disclose a method of increasing the magnetic flux density by promoting secondary recrystallization while applying a temperature gradient to the steel sheet.
- Patent Document 3 discloses a method of reducing iron loss by applying distortion to the steel sheet through scanning irradiation with an extremely finely focused laser beam.
- Patent Document 4 discloses a method of reducing iron loss by forming multiple grooves on the surface of the steel sheet.
- Patent Documents 1 and 2 increase magnetic flux density, but the secondary recrystallized grains grow coarse, resulting in poor iron loss characteristics if magnetic domain control technology is not applied.
- the technology of Patent Document 3 reduces iron loss, but the noise characteristics deteriorate because the amount of strain required for iron loss reduction is introduced into the steel sheet.
- the technology of Patent Document 4 reduces iron loss, but the magnetic flux density decreases because grooves of the depth required for iron loss reduction are formed in the steel sheet.
- the present invention has been made in consideration of the above problems.
- the object of the present invention is to provide a grain-oriented electrical steel sheet that is excellent in all of magnetic flux density, iron loss, and noise characteristics.
- the object of the present invention is to provide a grain-oriented electrical steel sheet that is excellent in all of magnetic flux density, iron loss, and noise characteristics, even when magnetic domain control technology is applied.
- the gist of the present invention is as follows:
- a grain-oriented electrical steel sheet is A grain-oriented electrical steel sheet having a base steel sheet and an insulating coating and having magnetic domain control,
- the magnetic flux density in the rolling direction when excited with 800 A/m is defined as B8 in units of T.
- the iron loss when excited to a magnetic flux density of 1.7 T at a frequency of 50 Hz is defined as W 17/50 in units of W/kg.
- the magnetostriction rate level calculated from the magnetostriction amount of the 200 Hz component of the magnetostriction waveform when excited to a magnetic flux density of 1.7 T at a frequency of 50 Hz is defined as Lva200@1.7 T in dB units
- the B8 satisfies B8 ⁇ 1.940
- the W 17/50 satisfies W 17/50 ⁇ 0.670
- the Lva200@1.7T satisfies ⁇ Lva200@1.7T ⁇ 46.0.
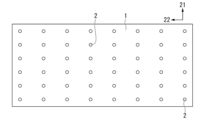
- FIG. 2 is a diagram showing an example of using spot current heating as a local rapid heating method, and is a schematic diagram showing an example of the arrangement of local heat affected regions in a decarburized annealed steel sheet.
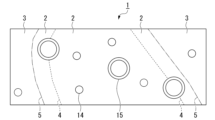
- FIG. 2 is a schematic diagram showing the distribution of Goss-oriented grains in a decarburized annealed steel sheet.
- the grain-oriented electrical steel sheet according to the present embodiment is a grain-oriented electrical steel sheet with controlled magnetic domains,
- the steel plate has a base material and an insulating coating.
- the magnetic flux density in the rolling direction when excited with 800 A/m is defined as B8 in units of T.
- the iron loss when excited to a magnetic flux density of 1.7 T at a frequency of 50 Hz is defined as W 17/50 in units of W/kg.
- the deviation between the crystal orientation of the secondary recrystallized grains and the ideal Goss orientation is controlled to be extremely small, and the secondary recrystallized grains are prevented from growing coarsely. Therefore, even if a magnetic domain control technique is applied, the energy density of the laser irradiation can be lowered and the depth of the grooves formed can be made shallower than in the conventional technique. As a result, the deterioration of noise characteristics caused by distortion due to laser irradiation and the decrease in magnetic flux density B8 caused by the formation of grooves can be preferably suppressed. Therefore, the grain-oriented electrical steel sheet according to this embodiment is excellent in all of magnetic flux density, iron loss, and noise characteristics (particularly the magnetostriction rate level in a medium magnetic field).
- multiple coarse Goss orientation grains close to the ideal Goss orientation are formed before secondary recrystallization, and these coarse Goss orientation grains are preferentially grown during secondary recrystallization, and the secondary recrystallization is terminated by causing these preferentially growing coarse Goss orientation grains to collide with each other. Therefore, in the grain-oriented electrical steel sheet according to this embodiment, the crystal orientation of the secondary recrystallized grains is close to the ideal Goss orientation, and the secondary recrystallized grains are fine. The manufacturing method of the grain-oriented electrical steel sheet according to this embodiment will be described later.
- the grain-oriented electrical steel sheet according to this embodiment has a magnetic flux density B8 of 1.940 T or more in the rolling direction.
- the magnetic flux density B8 is preferably 1.950 T or more, preferably 1.960 T or more, preferably 1.970 T or more, preferably 1.980 T or more, and more preferably 1.990 T or more.
- the magnetic flux density B8 when used as a wound core, the larger the magnetic flux density B8 , the more preferable it is, so there is no particular upper limit, but for example, the magnetic flux density B8 may be 2.00 T or less, or 1.99 T or less.
- the grain-oriented electrical steel sheet according to this embodiment has an iron loss W 17/50 of 0.670 W/kg or less.
- the value of the iron loss W 17/50 varies depending on the plate thickness t of the base steel plate. When the plate thickness t of the base steel plate becomes thinner, the value of the iron loss W 17/50 becomes smaller.
- the iron loss W 17/50 may be 0.670 W/kg or less regardless of the plate thickness.
- the iron loss W 17/50 is preferably 0.650 W/kg or less, and more preferably 0.600 W/kg or less.
- the smaller the value of the iron loss W 17/50 the more preferable it is, and the lower limit is not particularly limited.
- the iron loss value in the range where the above-mentioned Lva200@1.7T satisfies 46.0 dB or less becomes the lower limit of the iron loss W 17/50 .
- the lower limit of the iron loss W 17/50 may be set to 0.500 W/kg.
- the grain-oriented electrical steel sheet according to this embodiment has an Lva200@1.7T of 46.0 dB or less.
- the value of Lva200@1.7T varies depending on the magnetic flux density B8 .
- it is sufficient that Lva200@1.7T is 46.0 dB or less at any magnetic flux density B8 .
- Lva200@1.7T is preferably 45.0 dB or less, and preferably 40.0 dB or less.
- the smaller the value of Lva200@1.7T the more preferable it is, and the lower limit is not particularly limited.
- the lower limit of Lva200@1.7T may be 34.0 dB.
- the magnetic properties of the grain-oriented electrical steel sheet may be measured based on the single sheet magnetic property test method (SST: Single Sheet Tester) specified in JIS C 2556:2015. For example, 20 samples for single sheet magnetic measurement of 100 mm x 500 mm size are prepared from the grain-oriented electrical steel sheet, and the single sheet magnetic properties are measured.
- the magnetic flux density B 8 may be obtained as the magnetic flux density in the rolling direction of the steel sheet when excited at 800 A / m.
- the iron loss W 17 / 50 may be obtained as the iron loss defined as the power loss per unit weight (1 kg) of the steel sheet under the conditions of AC frequency: 50 Hz, excitation magnetic flux density: 1.7 T.
- magnetostriction ⁇ p-p@1.7T generated in the steel sheet may be measured under the conditions of AC frequency: 50 Hz and excitation magnetic flux density: 1.7 T.
- the magnetostriction rate level Lva200@1.7T can be calculated based on the magnetostriction characteristics described above.
- the magnetostriction rate level can be calculated using the following formula 1 by performing a Fourier transform on a magnetostriction waveform with two or more periods, acquired at a sampling frequency of 6.4 kHz, and using the magnetostriction amount ⁇ (fi) (0 Hz to 3.2 kHz) obtained for each frequency.
- Lva200@1.7T can be calculated with a frequency fi of 200 Hz.
- the grain-oriented electrical steel sheet according to the present embodiment is basically premised on the application of magnetic domain control technology for reducing iron loss.
- magnetic domain control technology for applying distortion by laser irradiation or the like when magnetic domain control technology for applying distortion by laser irradiation or the like is implemented, the noise characteristics of the transformer are deteriorated.
- the secondary recrystallized grain size can be made smaller than that of a conventional material having the same magnetic flux density B8 , so that the effect of reducing iron loss can be enjoyed even if the amount of distortion applied for magnetic domain refinement is reduced.
- the noise characteristics can be significantly improved while maintaining the same or higher iron loss characteristics.
- the grain-oriented electrical steel sheet according to this embodiment has a chemical composition that contains, by mass fraction, 2.0% to 7.0% Si, with the remainder being Fe and impurities.
- this grain-oriented electrical steel sheet may contain publicly known optional elements in place of a portion of Fe in order to improve the magnetic properties.
- the lower limit may be 0%.
- the upper limit for the optional elements may be set to a range in which no significant decrease in magnetic flux density or iron loss occurs. The approximate upper limit for each optional element is listed below.
- the grain-oriented electrical steel sheet (base steel sheet) has a chemical composition, in mass%, of: Si: 2.0 to 7.0%, C: 0 to 0.0050%, Mn: 0 to 1.0%, S and Se: 0 to 0.0150% in total, Al: 0 to 0.0650%, N: 0 to 0.0050%, Nb, V, Mo, Ta, and W: 0 to 0.050% in total; Cu: 0 to 0.40%, Bi: 0 to 0.010%, B: 0 to 0.080%, P: 0-0.50%, Ti: 0 to 0.0150%, Sn: 0 to 0.10%, Sb: 0 to 0.10%, Cr: 0 to 0.30%, Ni: 0-1.0%, and the remainder being Fe and impurities.
- Si 2.0-7.0%
- Silicon (Si) is a basic element for the base steel sheet. If the Si content is less than 2.0%, the eddy current loss cannot be sufficiently reduced, and good magnetic properties cannot be obtained.
- the Si content of the steel plate is 2.0% or more.
- the Si content is preferably 2.50% or more, and more preferably 3.0% or more.
- the Si content is 7.0%, If the Si content exceeds 7.0%, the steel sheet becomes brittle and the sheet passing property during production is significantly deteriorated, so the Si content of the base steel sheet is set to 7.0% or less.
- the Si content is preferably 4.50% or less. More preferably, it is 4.0% or less.
- C is an optional element for base steel plate.
- C is contained in the steel slab, but if excessive C remains in the base steel plate after final annealing, good core loss characteristics cannot be obtained. Therefore, the C content of the base steel sheet may be 0.0050% or less, preferably 0.0040% or less, and more preferably 0.0030% or less.
- the lower limit of the C content of the base steel sheet is not particularly limited and may be 0%. However, since it is not industrially easy to make the C content 0%, may be more than 0%, or may be 0.00010% or more.
- Mn 0 to 1.0%
- Mn manganese
- Mn is a selective element for the base steel sheet. Mn is contained in the steel slab, but if it is contained in excess, the steel undergoes phase transformation during secondary recrystallization annealing, secondary recrystallization does not proceed sufficiently, and good magnetic properties may not be obtained. Therefore, the Mn content of the base steel sheet may be 1.0% or less. The Mn content is preferably 0.50% or less, more preferably 0.20% or less.
- the lower limit of the Mn content of the base steel sheet is not particularly limited and may be 0%. However, since Mn forms MnS and MnSe and has the effect of acting as an inhibitor during secondary recrystallization, the Mn content may be more than 0% or may be 0.00010% or more.
- S and Se are selective elements for the base steel sheet.
- S and Se are contained in the steel slab, but if S and Se remain in excess in the base steel sheet after finish annealing, it may adversely affect the magnetic properties. Therefore, the total content of S and Se in the base steel sheet may be 0.0150% or less.
- the total content of S and Se is preferably 0.010% or less, more preferably 0.0050% or less.
- the lower limit of the total content of S and Se in the base steel sheet is not particularly limited and may be 0%. However, since S and Se form MnS and MnSe and have the effect of an inhibitor during secondary recrystallization, the total content of S and Se may be more than 0% or may be 0.00010% or more.
- Al is an optional element for base steel sheets. Al is contained in steel slabs, but if excessive Al remains in the base steel sheet after final annealing, it can adversely affect the magnetic properties. Therefore, the Al content of the base steel sheet may be 0.0650% or less. The Al content is preferably 0.040% or less, and more preferably 0.035% or less. The lower limit of the Al content of the base steel sheet is not particularly limited and may be 0%. However, since Al forms AlN and has an effect as an inhibitor during secondary recrystallization, the Al content is The amount of Al may be more than 0% or may be 0.00010% or more. Note that the above content of Al is acid-soluble Al (sol. Al).
- N is an optional element for base steel sheets.
- N is contained in the steel slab, but if excessive N remains in the base steel sheet after final annealing, it can adversely affect the magnetic properties. Therefore, the N content of the base steel sheet may be 0.0050% or less.
- the N content is preferably 0.0040% or less, and more preferably 0.0030% or less.
- the lower limit of the N content of the base steel sheet is not particularly limited and may be 0%. However, since N forms AlN and has an effect as an inhibitor during secondary recrystallization, the N content is The amount may be greater than 0% or may be 0.00010% or greater.
- Nb, V, Mo, Ta, and W are optional elements for the base steel plate. If an excessive amount of Nb group elements (one or more of Nb, V, Mo, Ta, and W) remains in the base steel plate, it may adversely affect the magnetic properties. Therefore, the total content of Nb, V, Mo, Ta, and W in the base steel plate may be 0.050% or less.
- the Nb group elements are preferably 0.030% or less, preferably 0.020% or less, and more preferably 0.010% or less.
- the total content of Nb, V, Mo, Ta, and W in the base steel plate is not particularly limited and may be 0%. However, since Nb, V, Mo, Ta, or W forms carbides, nitrides, or carbonitrides and has the effect of acting as an inhibitor during secondary recrystallization, the total content of Nb, V, Mo, Ta, and W may be more than 0% or may be 0.003% or more.
- Cu is an optional element for the base steel sheet. If the Cu content exceeds 0.40%, the steel sheet may become embrittled during hot rolling. Therefore, the Cu content of the base steel sheet is The Cu content is preferably 0.30% or less, and more preferably 0.10% or less. On the other hand, the lower limit of the Cu content is not particularly limited. However, since Cu has the effect of increasing the concentration of the Goss orientation and improving the magnetic properties, the Cu content may be more than 0%, and is set to 0.010% or more. Good too.
- Bi 0 ⁇ 0.010%
- Bi bismuth
- the Bi content of the base steel sheet may be 0.010% or less.
- the Bi content is preferably 0.0050% or less, and more preferably 0.0050% or less.
- the Bi content is 0.0020% or less, and more preferably 0.0010% or less.
- the lower limit of the Bi content is not particularly limited and may be 0%. However, Bi improves the magnetic flux density. Therefore, the Bi content may be set to more than 0% or to 0.00050% or more.
- B 0-0.080%
- B (boron) is an optional element for the base steel sheet. If the B content exceeds 0.080%, the variation (standard deviation) of the magnetic flux density may become large. Therefore, the B content is set to 0.
- the Bi content is preferably 0.070% or less, and more preferably 0.060% or less.
- the lower limit of the B content is not particularly limited, and is 0%. However, since B forms nitrides and has an effect as an inhibitor during secondary recrystallization, the B content may be more than 0% or may be 0.00050% or more. .
- P 0 to 0.50%
- P (phosphorus) is a selective element for the base steel sheet. If the P content exceeds 0.50%, the workability of the steel sheet may be significantly reduced. Therefore, the P content of the base steel sheet may be 0.50% or less.
- the P content is preferably 0.30% or less, more preferably 0.10% or less.
- the lower limit of the P content is not particularly limited and may be 0%. However, since P has the effect of improving the texture and improving the magnetic properties of the steel sheet, the P content may be more than 0% or may be 0.0020% or more.
- Ti 0 ⁇ 0.0150%
- Ti titanium is an optional element for the base steel plate. If the Ti content exceeds 0.0150%, the magnetic properties may be significantly reduced. Therefore, the Ti content of the base steel plate is set to 0.0150% or less.
- the Ti content is preferably 0.0130% or less, and more preferably 0.010% or less.
- the lower limit of the Ti content is not particularly limited, and is not limited to 0%. However, since Ti forms carbides, nitrides, and carbonitrides and has the effect of acting as an inhibitor during secondary recrystallization, the Ti content may be more than 0%, and may be less than 0.0020%. % or more.
- Sn 0-0.10%
- Sn (tin) is an optional element for the base steel sheet. If the Sn content exceeds 0.10%, the secondary recrystallization becomes unstable and may adversely affect the magnetic properties.
- the Sn content of the steel sheet may be 0.10% or less.
- the Sn content is preferably 0.090% or less, and more preferably 0.080% or less.
- the lower limit of the Sn content is However, since Sn has the effect of increasing the concentration of the Goss orientation and improving the magnetic properties, the Sn content may be more than 0%, and may be 0% or less. It may be 0.0050% or more.
- Sb 0-0.10%
- Sb antimony
- the Sb content of the base steel sheet is set to 0.10% or less.
- the Sb content is preferably 0.090% or less, and more preferably 0.080% or less.
- the lower limit of the Sb content is not particularly limited, and is not limited to 0%. However, since Sb functions as an inhibitor and has the effect of stabilizing secondary recrystallization, the Sb content may be more than 0% or may be 0.010% or more.
- Cr 0-0.30% Cr (chromium) is an optional element for the base steel plate. If the Cr content exceeds 0.30%, Cr oxides are formed, which may adversely affect the magnetic properties.
- the Cr content may be 0.30% or less.
- the Cr content is preferably 0.20% or less, and more preferably 0.10% or less.
- the lower limit of the Cr content is particularly However, since Cr has the effect of increasing the concentration of Goss orientation and improving magnetic properties, the Cr content may be more than 0%, and may be 0.010 % or more.
- Ni 0 to 1.0%
- Ni (nickel) is an optional element for the base steel plate. If the Ni content exceeds 1.0%, secondary recrystallization may become unstable. Therefore, the Ni content of the base steel plate may be 1.0% or less.
- the Ni content is preferably 0.20% or less, more preferably 0.10% or less.
- the lower limit of the Ni content is not particularly limited and may be 0%. However, since Ni has the effect of increasing electrical resistance and reducing iron loss, the Ni content may be more than 0% or may be 0.010% or more.
- the base steel sheet of the grain-oriented electrical steel sheet according to this embodiment may contain impurities.
- impurities refer to substances that are mixed in from raw materials such as ore or scrap during industrial production of steel, or from the production environment, etc.
- the chemical composition of the above-mentioned base steel plate may be measured by a general analytical method. For example, it may be measured using ICP-AES (Inductively Coupled Plasma-Atomic Emission Spectrometry). Acid-soluble Al may be measured by ICP-AES using the filtrate after thermally decomposing the sample with acid. C and S may be measured using the combustion-infrared absorption method, N using the inert gas fusion-thermal conductivity method, and O using the inert gas fusion-non-dispersive infrared absorption method.
- ICP-AES Inductively Coupled Plasma-Atomic Emission Spectrometry
- Acid-soluble Al may be measured by ICP-AES using the filtrate after thermally decomposing the sample with acid.
- C and S may be measured using the combustion-infrared absorption method, N using the inert gas fusion-thermal conductivity method, and O using the inert gas fusion-non-dispersive infrared absorption
- the above chemical composition is that of the base steel sheet. If the grain-oriented electrical steel sheet to be used as the measurement sample has an insulating coating on its surface, the coating is removed using the method described below before measuring the chemical composition.
- the insulating coating can be removed by immersing the grain-oriented electrical steel sheet having the coating in a high-temperature alkaline solution.
- the insulating coating can be removed from the grain-oriented electrical steel sheet by immersing the sheet in an aqueous sodium hydroxide solution containing 30 to 50 mass % NaOH and 50 to 70 mass % H 2 O at 80 to 90° C. for 5 to 10 minutes, followed by rinsing with water and drying.
- the time for immersion in the aqueous sodium hydroxide solution can be changed depending on the thickness of the insulating coating.
- the electrical steel sheet from which the insulating coating has been removed using the above method may be immersed in hot hydrochloric acid.
- the preferred concentration of hydrochloric acid for removing the forsterite coating to be dissolved is determined in advance, and the forsterite coating can be removed by immersing the sheet in hydrochloric acid of this concentration (e.g. 30-40% by mass hydrochloric acid) at 80-90°C for 1-5 minutes, followed by rinsing with water and drying.
- different treatment solutions are used to remove each coating, such as using an alkaline solution to remove the insulating coating and hydrochloric acid to remove the forsterite coating.
- a grain-oriented electrical steel sheet with excellent quality can be obtained by performing localized rapid heating on a cold-rolled steel sheet to form a localized heated region, followed by primary annealing (decarburization annealing) and secondary annealing (finish annealing).
- the locally heated region formed before the primary annealing is located locally on the surface of the steel plate.
- the crystalline structure of this locally heated region consists of one or both of a recrystallized structure and a recovered structure at the end of the local rapid heating.
- the crystalline structure of the non-rapidly heated parts of the steel plate surface other than the locally heated region consists of a cold worked structure that remains as it is cold rolled.
- the above-mentioned localized rapid heating has a heating rate of 500°C/sec or more, preferably 2000°C/sec or more, and more preferably 10000°C/sec or more.
- a heating rate 500°C/sec or more, preferably 2000°C/sec or more, and more preferably 10000°C/sec or more.
- the frequency of coarse Goss orientation grains in the localized heating affected area is greater than that obtained by normal rapid heating of the entire plate. This characteristic is thought to be due to the fact that the peripheral area of the locally heated area is a processed structure that retains a lot of distortion. Specifically, when localized rapid heating is performed, the practical Goss orientation grains generated in the locally heated area preferentially encroach on the peripheral unrecrystallized area that retains a lot of distortion during the primary annealing, and grow in diameter. However, when the entire steel plate is heated, the generation and growth of recrystallized grains occurs uniformly within the steel plate, so it is thought that the above-mentioned enlargement does not occur.
- the Goss-oriented grains formed in the local heat-affected zone grow preferentially during secondary annealing.
- Many Goss-oriented grains are formed in the local heat-affected zone, including Goss-oriented grains that have a particularly small angular deviation, are close to the ideal Goss orientation, and have large crystal grain sizes after primary annealing. During secondary recrystallization, these Goss-oriented grains grow preferentially.
- Goss orientation grains that serve as the nuclei for secondary recrystallization are supplied to the local heat affected region, there is no need to form Goss orientation grains in the primary annealing in the matrix parts other than the local heat affected region, i.e., the local heat unaffected region. Therefore, as the heat treatment conditions for the primary annealing, a slow heating condition with a low heating rate may be adopted, which forms many corresponding orientation grains with the ⁇ 111 ⁇ 112> and ⁇ 411 ⁇ 148> orientations that are easily eroded in the local heat unaffected region.
- the heating rate for the primary annealing to 300°C/sec or less, many Goss orientation grains with large crystal grain size and close to the ideal Goss orientation are formed in the local heat affected region, while almost no Goss orientation grains are formed in the local heat unaffected region, and conversely, many corresponding orientation grains can be formed.
- the Goss orientation grains that are present in the local heat affected zone are close to the ideal Goss orientation, and have a large grain size begin preferential growth and grow toward the zone not affected by the local heat. If the Goss orientation grains that have begun preferential growth collide with other Goss orientation grains that have begun to grow from the adjacent local heat affected zone, the grain growth stops.
- the coarse Goss orientation grains that are close to the ideal Goss orientation and grow preferentially are favorably arranged in the steel sheet, and as a result, the grain size of the Goss orientation grains at the end of secondary annealing is reduced. In other words, a secondary recrystallized structure with a fine grain size can be obtained, despite having a crystal orientation close to the ideal Goss orientation.
- spot current heating by electrical resistance heating is described below.
- spot current heating spot electrodes are pressed against both sides of a steel sheet, and current is passed between the spot electrodes to spot current heat the electrode holding portion of the steel sheet.
- a steel having the composition shown in Table 1 was used, and a cold-rolled steel sheet with a sheet thickness of 0.22 mm was obtained by hot rolling and cold rolling. This steel sheet was subjected to spot current heating.
- the spot current heating was performed using a copper electrode with a diameter of 3 mm, under the following conditions: current of 5.0 kA or less, which is a range in which the steel sheet surface does not melt, current time of 20 milliseconds to 80 milliseconds, electrode pressure of 50 kgf to 150 kgf, and electrode holding time after current application of 0.2 seconds.
- Spot current heating was performed on the surface of the cold-rolled steel sheet in a grid pattern with a pitch of 20 mm in the rolling direction and a pitch of 30 mm in the width direction (perpendicular to the rolling direction), forming a localized heating area.
- This cold-rolled steel sheet was subjected to decarburization annealing (primary annealing). In the decarburization annealing, the cold-rolled steel sheet was heated at a heating rate of 20°C/sec and held at 830°C for 90 seconds.
- Figure 1 shows an example of the arrangement of local heat affected areas in a decarburized annealed steel sheet manufactured under the above conditions.
- the decarburized annealed steel sheet 1 the local heat affected areas 2, the rolling direction 21, and the width direction (direction perpendicular to the rolling direction) 22 are shown diagrammatically.
- FIG. 1 is a schematic diagram showing the distribution of Goss orientation grains in the decarburized annealed steel sheet manufactured under the above conditions.
- the current-carrying electrode used for spot current heating is circular, and its diameter is preferably 0.5 mm ⁇ to 10 mm ⁇ , and more preferably 1 mm ⁇ to 5 mm ⁇ , in terms of circle equivalent diameter. Note that, although a circular current-carrying electrode was used in the above, it is sufficient to locally increase the heating rate of the cold-rolled steel sheet, form Goss-oriented grains in this region, and allow the grains to grow; the electrode shape may be other shapes, for example, elliptical or linear.
- the decarburized annealed steel sheet 1 manufactured under the above conditions contains Goss orientation grains 14 as well as coarse Goss orientation grains 15.
- the region containing the coarse Goss orientation grains 15 corresponds to the local heat affected region 2.
- Figure 2 shows a schematic of the local heat affected region boundary 4 and the local heat affected region boundary 5, it is not easy to distinguish these boundaries by observing the structure.
- the region containing the coarse Goss orientation grains 15 can be considered to be the local heat affected region 2.
- the above decarburized annealed steel sheets were further nitrided, coated with an annealing separator mainly composed of MgO, and then subjected to secondary annealing.
- the secondary annealing conditions were: hydrogen nitrogen atmosphere, heating rate: 15°C/hr (°C/hr), holding: 1200°C-20hr (hr).
- the obtained steel plate was subjected to macro-etching to reveal the grain boundaries.
- macro-etching was observed at the locations corresponding to the local heat affected areas, it was found that in some cases multiple secondary recrystallized grains had grown from the locations corresponding to the local heat affected areas, and in other cases secondary recrystallized grains had spread from the center of the locations corresponding to the local heat affected areas.
- minute grains of 2 mm or less were sometimes observed as traces of the local heat affected areas, but in other cases they were not.
- the secondary recrystallized macrostructure may change slightly depending on the local heating conditions, the degree of accumulation in the Goss orientation was increased compared to when local heat treatment was not performed.
- the obtained grain-oriented electrical steel sheet had an extremely small deviation between the crystal orientation of the secondary recrystallized grains and the ideal Goss orientation, and that the grains did not grow coarsely.
- magnetic domain control technology was applied to this grain-oriented electrical steel sheet, and it was confirmed that the magnetic flux density B8 was 1.940 T or more, the iron loss W17 /50 was 0.670 W/kg or less, and the Lva200@1.7 T was 46.0 dB or less.
- the coarse Goss orientation grains (Goss orientation grains with large crystal grain size) close to the ideal Goss orientation grow preferentially. Therefore, even if the secondary recrystallized grains are not allowed to grow large, it is possible to obtain a steel sheet dominated by secondary recrystallized grains close to the ideal Goss orientation.
- the size, shape, and arrangement of the crystal grains after secondary annealing can be controlled by appropriately arranging the local heat affected zones on the steel sheet surface.
- the grain size of the Goss orientation grains at the end of secondary annealing will be small, and a steel sheet with excellent iron loss can be obtained.
- the Goss orientation grains that grow preferentially from the local heat-affected region have a crystal orientation close to the ideal Goss orientation, so good magnetic flux density can be obtained despite the small secondary recrystallized grain size.
- the above-mentioned grain-oriented electrical steel sheet can increase the magnetic flux density while suppressing the coarsening of the secondary recrystallized grain size, and therefore can reduce the introduction of strain and the formation of grooves for the magnetic domain width refinement.
- the energy density of the laser irradiation can be lowered and the depth of the grooves formed can be made shallower than in the conventional technology. Therefore, compared to the conventional technology, the increase in the magnetostriction rate level Lva caused by the strain of the laser irradiation and the decrease in the magnetic flux density B8 caused by the formation of grooves can be preferably suppressed.
- the method for manufacturing the grain-oriented electrical steel sheet according to this embodiment is not limited to the method described below.
- the manufacturing method described below is one example for manufacturing the grain-oriented electrical steel sheet according to this embodiment.
- the steps and quantitative conditions for each step shown below are examples adopted to demonstrate the feasibility of this embodiment, and this embodiment is not limited to these steps and quantitative values.
- the manufacturing method for grain-oriented electrical steel sheet according to this embodiment may adopt various conditions as long as they do not deviate from the gist of this embodiment and achieve the purpose of this embodiment.
- the manufacturing method of the grain-oriented electrical steel sheet according to this embodiment can apply the conventional known manufacturing method of grain-oriented electrical steel sheet as a basic process.
- examples of conventional manufacturing methods of grain-oriented electrical steel sheet include a manufacturing method in which inhibitors such as MnS and AlN are formed by high-temperature slab heating, and a manufacturing method in which AlN inhibitors are formed by low-temperature slab heating and nitriding treatment.
- the manufacturing method of the grain-oriented electrical steel sheet according to this embodiment is not limited to a specific manufacturing method. Below, a method of applying nitriding treatment as a low-temperature slab heating process will be described.
- a slab is prepared.
- An example of a method for producing a slab is as follows. Molten steel is produced (smelted). A slab is produced using the molten steel. The slab may be produced by a continuous casting method. An ingot may be produced using the molten steel, and the ingot may be bloomed to produce a slab.
- the thickness of the slab is not particularly limited. The thickness of the slab is, for example, 150 to 350 mm. The thickness of the slab is preferably 220 to 280 mm. As the slab, a so-called thin slab having a thickness of 10 to 70 mm may be used. When a thin slab is used, rough rolling before finish rolling can be omitted in the hot rolling process.
- the above slab may contain the following elements in its chemical composition:
- Carbon (C) is an effective element for controlling the primary recrystallized structure in the manufacturing process, but if its content in the final product is excessive, it will have a detrimental effect on the magnetic properties.
- the preferred upper limit of the C content is 0.075%.
- C is purified in the decarburization annealing process and the finish annealing process to be 0.005% or less.
- the lower limit of the C content may be more than 0%, or may be 0.001%.
- Si 2.0-7.0%
- Silicon (Si) increases the electrical resistance of grain-oriented electrical steel sheets and reduces iron loss. If the Si content is less than 2.0%, ⁇ transformation occurs during final annealing, and the crystallization of the grain-oriented electrical steel sheets is reduced. On the other hand, if the Si content exceeds 7.0%, the cold workability decreases and cracks tend to occur during cold rolling.
- the upper limit of the Si content is preferably 4.5%, and more preferably 4.0%.
- Mn 0.05-1.00%
- Manganese (Mn) combines with S or Se to produce MnS or MnSe, and functions as an inhibitor.
- Mn is contained, the Mn content is within the range of 0.05 to 1.00%.
- the secondary recrystallization is stable. It is possible for part of the inhibitor function to be performed by a nitride of an Nb group element. In this case, the strength of MnS or MnSe as a general inhibitor is Therefore, the upper limit of the Mn content is preferably 0.50%, and more preferably 0.20%.
- At least one of S and Se 0.003 to 0.035% in total Sulfur (S) and selenium (Se) combine with Mn to produce MnS or MnSe, which functions as an inhibitor.
- S and Se When at least one of S and Se is contained, if the total content of S and Se is 0.003 to 0.035%, secondary recrystallization is stable. It is possible for a part of the inhibitor function to be borne by a nitride of an Nb group element. In this case, the strength of MnS or MnSe as a general inhibitor is controlled to be weak. For this reason, the preferred upper limit of the total content of S and Se is 0.025%, and more preferably 0.010%. If S and Se remain after the final annealing, they form compounds and deteriorate the iron loss. Therefore, it is preferable to reduce S and Se as much as possible by purification during the final annealing.
- the total content of S and Se means that at least one of S and Se is included, and is the total content.
- Al 0.010-0.065%
- Aluminum (Al) combines with N to precipitate as (Al,Si)N, and functions as an inhibitor.
- the Al content is within the range of 0.010 to 0.065%.
- AlN formed as an inhibitor by nitriding, which will be described later expands the secondary recrystallization temperature range, and secondary recrystallization is particularly stable in the high temperature range. Therefore, the Al content is 0.010 to 0.065
- the lower limit of the Al content is preferably 0.020%, and more preferably 0.025%.
- the upper limit of the Al content is preferably 0.040%. and more preferably 0.035%.
- N 0.012% or less Nitrogen (N) combines with Al to function as an inhibitor. Since N can be contained by nitriding during the manufacturing process, no lower limit is specified. For example, the lower limit of the N content may be more than 0%, or may be 0.001%. On the other hand, when N is contained, if the N content exceeds 0.012%, blisters, which are a type of defect, tend to occur in the steel sheet. The preferred upper limit of the N content is 0.010%, and more preferably 0.009%. N is purified in the final annealing process, and becomes 0.005% or less after the final annealing process.
- the balance of the above chemical composition consists of Fe and impurities.
- impurities refers to elements that are mixed in from raw materials such as ore and scrap during industrial production of steel, or from the production environment, etc.
- the upper limit of the total impurity content may be, for example, 5%.
- the above-mentioned chemical composition may contain known optional elements in place of part of Fe, taking into consideration not only solving manufacturing problems, but also strengthening the inhibitor function through compound formation and the effect on magnetic properties.
- optional elements that may be contained in place of part of Fe include the following elements:
- Nb group elements 0.050% or less
- the total content of Nb group elements (one or more of Nb, V, Mo, Ta, and W) may be 0.050% or less.
- the total content of Nb group elements is 0.030% or less, since secondary recrystallization is started at an appropriate timing.
- the orientation of the secondary recrystallized grains generated becomes very favorable, and the structure can be finally controlled to be favorable for magnetic properties.
- Nb and Ta have a strong effect and are preferable.
- the total content of Nb group elements is more preferably 0.004 to 0.020%. Even more preferably, it is 0.005 to 0.010%.
- the total content of Nb group elements means the total content including at least one of Nb, V, Mo, Ta, and W.
- the slab also contains, as optional elements, in mass %: Cu: 0.40% or less, Bi: 0.010% or less, B: 0.080% or less, P: 0.50% or less, Ti: 0.015% or less, Sn: 0.10% or less, Sb: 0.10% or less, Cr: 0.30% or less, Ni: 1.00% or less. Since these optional elements may be contained according to known purposes, there is no need to set a lower limit for the content of the optional elements, and the lower limit may be 0%.
- the chemical composition of the above slabs can be measured by the above analytical method, just like the chemical composition of the final product, grain-oriented electrical steel sheet.
- the hot rolling process is a process in which a slab heated to a predetermined temperature (e.g., 1100 to 1400°C) is hot-rolled to obtain a hot-rolled steel sheet.
- a predetermined temperature e.g. 1100 to 1400°C
- the silicon steel material (slab) heated in the heating process is roughly rolled, and then finish-rolled to obtain a hot-rolled steel sheet with a predetermined thickness, for example, 1.8 to 3.5 mm. After the finish rolling is completed, the hot-rolled steel sheet is coiled at a predetermined temperature.
- the slab heating temperature should be 1100°C to 1280°C.
- the hot-rolled sheet annealing process is a process in which the hot-rolled steel sheet obtained in the hot rolling process is annealed under a predetermined temperature condition (for example, at 750 to 1200 ° C for 30 seconds to 10 minutes) to obtain an annealed steel sheet.
- Hot-rolled sheet annealing is generally performed to control the steel sheet structure such as the recrystallization rate, residual strain, and crystal grain size by annealing the hot-rolled steel sheet after the hot rolling process, and to preferably adjust the precipitate form in the steel.
- a high-temperature slab heating process it is a process for finally controlling the form of precipitates such as AlN, and conditions are adjusted so that they precipitate uniformly and finely.
- the hot-rolled sheet annealing for example, after heating the steel sheet to 1050 ° C to 1150 ° C, in order to properly precipitate AlN, etc., it may be cooled slowly to an intermediate temperature (850 ° C to 950 ° C) for 50 to 150 seconds, and then cooled with water.
- an intermediate temperature 850 ° C to 950 ° C
- the cold rolling process is a process in which the annealed steel sheet obtained in the hot-rolled sheet annealing process is subjected to one cold rolling or multiple cold rolling (two or more times) via annealing (intermediate annealing) to obtain a cold-rolled steel sheet having a thickness of, for example, 0.10 to 0.50 mm.
- the interpass temperature of the cold rolling may be set to about 100° C. to 300° C.
- local rapid heating is performed on the cold-rolled steel sheet after the cold rolling process to form a local heating region.
- the rapid heating method is not particularly limited as long as it can locally heat the steel sheet.
- a method of heating by contacting a spot electrode with the front and back surfaces of the steel sheet and passing an electric current through the steel sheet a method of heating by irradiating the surface of the steel sheet with laser light or an electron beam, a method of locally heating by induction heating, a method of heating by contacting a hot piece, etc. can be adopted.
- each local heating region can be a dot-like region with a diameter of about 10 ⁇ m to 10 mm, or a linear region with a width of about 10 ⁇ m to 10 mm.
- the electrode used for current heating may be a circular electrode as described above, or a linear electrode.
- the minimum diameter and width of the locally heated region depend on the shape of the spot electrode and the technology for reducing the focused diameter of the laser light or electron beam. In principle, it is possible to further reduce the size of the locally heated region, but considering that the current size of the recrystallized grain nuclei is about 1 ⁇ m, it is believed that an effect can be obtained if the size of the locally heated region is 1 ⁇ m or more. From an industrial perspective, the above minimum diameter and width should be 10 ⁇ m or more. Furthermore, if the maximum diameter or width of the locally heated region exceeds 10 mm, the area proportion of Goss orientation grains with a relatively large angle deviation that cannot grow outside the locally heated region increases. In this case, it becomes difficult to obtain the effect of local rapid heating.
- the heating rate should be 500°C/sec or more in the center of the locally heated region as viewed in the thickness direction and at 1/5 of the thickness of the steel plate. If the heating rate in the above region is 500°C/sec or more, the structure of the locally heated region can be preferably controlled to a recovered structure or a recrystallized structure.
- the above heating rate is preferably 2000°C/sec or more, and more preferably 10000°C/sec or more.
- the upper limit of the above heating rate is not particularly limited, and may be, for example, 1,000,000°C/sec.
- the aim is to have coarse Goss oriented grains in the local heat affected region after decarburization annealing, but if the heating rate during decarburization annealing is faster than the heating rate during local rapid heating, it is difficult to achieve the above objective. Therefore, although it depends on the magnitude of the heating rate, it is preferable to set the heating rate during local rapid heating to be equal to or higher than the heating rate during decarburization annealing.
- the 1/5 part of the thickness of the steel plate mentioned above refers to a depth equivalent to 1/5 of the thickness of the steel plate from the surface of the steel plate in the thickness direction.
- the maximum temperature reached should be 700°C or higher in the center of the locally heated region when viewed from the plate thickness direction and at 1/5 of the plate thickness of the steel plate. If the maximum temperature reached in the above region is 700°C or higher, the structure of the locally heated region can be preferably controlled to a recovered structure or a recrystallized structure.
- the above maximum temperature reached is preferably 800°C or higher, and more preferably 900°C or higher.
- the above maximum temperature reached should be below the melting point of the steel plate, for example, 1400°C or lower.
- the holding time from reaching the maximum temperature to cooling to 700°C at the center of the locally heated region as viewed from the thickness direction and at 1/5 of the thickness of the steel plate should be 0.1 seconds or more. If the holding time in the above region is 0.1 seconds or more, the structure of the locally heated region can be preferably controlled to a recovered structure or a recrystallized structure.
- the holding time is preferably 0.2 seconds or more, more preferably 0.3 seconds or more, and even more preferably 0.4 seconds or more.
- there is no particular limit to the upper limit of the holding time and it may be, for example, 10 seconds or less.
- the holding time from reaching the maximum temperature to cooling to 700°C has a fundamental effect on the formation of coarse Goss orientation grains close to the ideal Goss orientation.
- the method of local rapid heating is not particularly limited.
- local rapid heating may be performed by spot electrical current heating, laser irradiation, or electron beam irradiation.
- it is sufficient to control the heating rate, maximum temperature, and holding time described above so as to satisfy the above.
- a person skilled in the art can combine the various conditions of the local rapid heating method to control the desired heating rate, maximum temperature, and holding time.
- a person skilled in the art can perform a heat conduction analysis using the finite element method to control the heating rate and maximum temperature reached in the center of the localized heating area when viewed from the plate thickness direction and at 1/5 of the plate thickness of the steel plate.
- a person skilled in the art can control the above-mentioned holding time by adjusting the heat removal conditions after the maximum temperature is reached. For example, in the case of spot current heating, the electrode holding time after current is controlled, or the shape of the spot electrode can be changed to a shape suitable for heat removal.
- the irradiation speed can be adjusted, or the shape of the irradiation area can be changed to an ellipse or the like to gradient the irradiation energy from the center to the outer edge of the irradiation area.
- the heating by laser irradiation preferentially heats only the vicinity of the irradiated steel sheet surface, and the inside of the steel sheet is not easily heated.
- the heating by laser irradiation is non-contact heating, the heat is removed quickly after heating, and the temperature is not easily maintained. Therefore, when performing laser irradiation heating as local rapid heating, in order to recover or recrystallize the cold-worked structure in the laser irradiated region, it is necessary to control the conditions so that not only the surface of the steel sheet but also the inside of the steel sheet is heated, and the cooling rate is slowed down to relatively coarsen the subgrain structure in the laser irradiated region.
- the laser irradiation conditions for performing local rapid heating are completely different from the laser irradiation conditions for performing magnetic domain refinement. For example, even if the laser irradiation conditions for performing magnetic domain refinement (usually 0.5 to 50 mJ/mm 2 ) are applied to this embodiment, the structure of the locally heated region is not favorably controlled, and coarse Goss orientation grains close to the ideal Goss orientation are not formed in the steel sheet after the decarburization annealing process. The same applies to electron beam irradiation as to laser irradiation.
- the structure of the locally heated region is not favorably controlled, and coarse Goss oriented grains close to the ideal Goss orientation are not formed in the steel sheet after the decarburization annealing process.
- decarburization annealing process In the decarburization annealing step, the cold-rolled steel sheet after the local rapid heating step is subjected to decarburization annealing (primary annealing). This decarburization annealing increases the frequency of Goss-oriented grains formed in the local heat-affected zone, increases the grain size of the Goss-oriented grains, and preferably forms coarse Goss-oriented grains having an orientation close to the ideal Goss orientation.
- the decarburization annealing conditions may be a heating rate of 10 to 10,000°C/sec, an annealing temperature of 700 to 900°C, and an annealing time of 10 to 600 seconds.
- C contained in the cold-rolled steel sheet is removed. It is preferable to perform the decarburization annealing in a moist atmosphere in order to remove "C" contained in the cold-rolled steel sheet.
- the primary recrystallized grain size is not particularly limited, but is preferably 8 to 30 ⁇ m.
- the heating rate of decarburization annealing may be 10,000°C/sec or less, but it is preferable to slow down the heating rate of decarburization annealing to form ⁇ 111 ⁇ 112> orientation grains and ⁇ 411 ⁇ 148> orientation grains that are easily eroded into the matrix portion (region not affected by local heat).
- the heating rate of decarburization annealing is preferably 300°C/sec or less, more preferably 200°C/sec or less, and even more preferably 100°C/sec or less.
- the degree of oxidation (PH 2 O/PH 2 ) in the annealing atmosphere may be set to 0.01 to 0.15.
- the degree of oxidation PH 2 O/PH 2 can be defined as the ratio of the water vapor partial pressure PH 2 O to the hydrogen partial pressure PH 2 in the atmosphere.
- Nitriding is an effective treatment in a low-temperature slab heating process in which the slab heating temperature is 1280°C or less, and is an important step for adjusting the strength of the inhibitor in secondary recrystallization. Nitriding increases the nitrogen content of the steel sheet by about 40 to 200 ppm between the start of the decarburization treatment and the start of secondary recrystallization in the finish annealing.
- Examples of nitriding include a treatment of annealing in an atmosphere containing a gas with nitriding ability such as ammonia, and a treatment of finish annealing a decarburized annealed steel sheet coated with an annealing separator containing a powder with nitriding ability such as MnN.
- the amount of nitriding after the nitriding treatment is preferably 130 to 350 ppm, and more preferably 150 to 250 ppm.
- the annealing separator application process is a process of applying an annealing separator to the decarburized annealed steel sheet.
- an annealing separator mainly composed of MgO or an annealing separator mainly composed of Al 2 O 3 can be used.
- the decarburized annealed steel sheet after application of the annealing separator is wound into a coil and is finish annealed in the next finish annealing process.
- the final annealing process is a process in which the decarburized annealed steel sheet coated with the annealing separator is subjected to final annealing (secondary annealing) to cause secondary recrystallization.
- second annealing final annealing
- the growth of the primary recrystallized grains is suppressed by an inhibitor, and the secondary recrystallization is allowed to proceed, thereby preferentially growing ⁇ 100 ⁇ 001> oriented grains and dramatically improving the magnetic flux density.
- the decarburized annealed steel sheet that has been coated with an annealing separator and dried may be held at a temperature range of 1000°C to 1300°C for 10 hours to 60 hours.
- the atmosphere during the final annealing may be, for example, a nitrogen atmosphere or a mixed atmosphere of nitrogen and hydrogen.
- secondary recrystallization may be caused by applying a temperature gradient of more than 0.5°C/cm to the boundary between the primary recrystallized region and the secondary recrystallized region in the steel sheet during the heating process of the finish annealing, preferably by applying a temperature gradient of 1.0°C/cm or more.
- the above temperature gradient may be applied to the steel sheet during the growth of secondary recrystallized grains in a temperature range of 800°C or more during the heating process of the finish annealing.
- the direction in which the above temperature gradient is applied may be the direction C perpendicular to the rolling.
- the above temperature gradient may be changed appropriately depending on the chemical composition of the steel.
- the temperature gradient may be more than 0.5°C/cm (preferably 1.0°C/cm or more), while if the chemical composition is such that secondary recrystallized grains tend not to grow preferentially, the temperature gradient is preferably more than 1.0°C/cm.
- the method of providing a temperature gradient is not particularly limited, and any known method may be applied.
- the position and arrangement of the heating device and the temperature distribution in the annealing furnace may be controlled so that a sufficient temperature difference is generated from the top to the bottom of the coil, or from the outside to the inside.
- a temperature distribution may be formed in the coil being annealed by actively heating only a portion of the coil using induction heating, high-frequency heating, or electrical heating devices.
- secondary recrystallized grains with sharp orientations will be generated from the parts of the coil that have reached the secondary recrystallization start state early, and these secondary recrystallized grains will grow preferentially due to the temperature gradient.
- the secondary recrystallized grains can be made to grow throughout the entire coil.
- a coating solution containing phosphoric acid or a phosphate, chromic anhydride or a chromate, and colloidal silica is applied to the steel sheet after the final annealing and baked (for example, at 350° C. to 1150° C. for 5 to 300 seconds), An insulating coating is formed.
- a localized micro-distortion region or a localized groove is formed on the steel sheet by a known method such as laser, plasma, mechanical method, or etching.
- strain may be imparted to the steel sheet by irradiating it with a laser or electron beam. Irradiation with the laser or electron beam may not melt the steel sheet, or may only partially melt the steel sheet.
- the method of forming localized grooves in a steel sheet is not particularly limited.
- the steel sheet may be irradiated with a laser or electron beam, and the steel in the irradiated area may be melted and evaporated to form the grooves.
- a gear may be pressed onto the surface of the steel sheet to mechanically form the grooves.
- a resist film with predetermined holes may be printed on the surface of the steel sheet, and the grooves may be formed by electrolytic etching.
- the grooves may be formed at any known time point after the cold rolling process.
- the above-mentioned distortions and grooves are arranged in a line or dot shape extending in a direction intersecting the rolling direction on the rolled surface of the steel sheet, and are spaced 2 mm to 10 mm apart in the rolling direction.
- the above-mentioned distortions may be locally applied to the steel sheet so that the energy density Ua is 0.1 to 10 mJ/ mm2 and the irradiation diameter is 10 to 500 ⁇ m.
- the above-mentioned grooves may be locally formed in the steel sheet so that the groove depth is 10 to 50 ⁇ m.
- the energy density of the laser irradiation can be lowered or the depth of the grooves formed can be made shallower, as compared with the conventional technology.
- a person skilled in the art understands the objective of "improving iron loss characteristics while preferably suppressing an increase in the magnetostriction rate level Lva caused by distortion due to laser irradiation and a decrease in the magnetic flux density B8 caused by the formation of grooves", he or she can preferably control the magnetic domain control conditions within the above-mentioned numerical ranges according to the target secondary recrystallized structure.
- the grain-oriented electrical steel sheet it is possible to determine whether the magnetic domains are controlled, that is, whether the steel sheet has localized distortion or localized grooves, by the following method.
- the coating may be removed by the method described above. The surface of the electrical steel sheet from which the coating has been removed is observed visually or under a microscope. If linear or dot-like grooves are present on the steel sheet surface at intervals of 2 mm to 10 mm, the steel sheet is determined to have localized grooves.
- the steel sheet is determined to have localized distortion.
- a person skilled in the art would be able to determine whether linear or dot-like grooves or laser or electron beam irradiation marks are localized distortion or localized grooves for magnetic domain refinement.
- the sample is heat-treated at 800°C for 120 minutes, and the iron loss values before and after the heat treatment are compared. If the iron loss W17 /50 value increases by 0.02 W/kg or more due to this heat treatment, it can be determined that the steel sheet before the heat treatment has localized distortion.
- the grain-oriented electrical steel sheet according to this embodiment can be manufactured by the above process.
- the grain-oriented electrical steel sheet according to this embodiment which is manufactured by controlling the conditions of each process in a complex and inseparable manner, has an extremely small deviation between the crystal orientation of the secondary recrystallized grains and the ideal Goss orientation, and the crystal grains do not grow coarsely. Therefore, even if magnetic domain control technology is applied, the magnetic flux density, core loss, and noise characteristics are all excellent.
- the grain-oriented electrical steel sheet according to this embodiment when manufacturing the grain-oriented electrical steel sheet according to this embodiment, it is assumed that local rapid heating is performed on the cold-rolled steel sheet, but other manufacturing conditions may be optimized depending on the purpose. For example, if the distance between the rolling direction L and the direction perpendicular to the rolling direction C of the local rapid heating is reduced, the grain-oriented electrical steel sheet according to this embodiment can be manufactured without relaxing manufacturing conditions other than the local rapid heating and controlling the temperature gradient during the heating process of the finish annealing.
- the grain-oriented electrical steel sheet according to this embodiment can be manufactured by controlling the temperature gradient during the heating process of the finish annealing or by controlling the steel composition to a chemical composition that facilitates preferential growth of secondary recrystallized grains. If a person skilled in the art understands the characteristics of the grain-oriented electrical steel sheet according to this embodiment described above, he or she can preferably optimize the local rapid heating conditions and other manufacturing conditions.
- the conditions in the examples are one example of conditions adopted to confirm the feasibility and effects of the present invention, and the present invention is not limited to this one example of conditions.
- Various conditions can be adopted in the present invention as long as they do not deviate from the gist of the present invention and the object of the present invention is achieved.
- the chemical composition-adjusted slabs were used as the raw material to manufacture decarburized annealed steel sheets with the chemical compositions shown in Table 2. These chemical compositions were measured based on the method described above. In Table 2, "-" indicates that no control or manufacturing was carried out with the content in mind, and that no content measurements were carried out.
- the slabs were heated to 1150°C and subjected to hot rolling to obtain hot-rolled steel sheets with a thickness of 2.6 mm.
- the hot-rolled steel sheets were then heated to 1100°C and subsequently annealed at 900°C for hot-rolled sheet annealing, after which the sheets were pickled to remove the scale formed on the surface.
- These steel sheets were subjected to one cold rolling or multiple cold rolling with intermediate annealing in between to obtain cold-rolled steel sheets with a final thickness of 0.22 mm.
- the above cold-rolled steel sheets were subjected to localized rapid heating under the conditions shown in Tables 3 to 10.
- spot current heating a copper electrode with a diameter of 1 mm was used in contact with the steel sheet, and the electrode shape, electrode pressure, current, current duration, and electrode holding time after current were varied in a composite manner to control the heating rate, maximum temperature, and holding time from reaching the maximum temperature until cooling to 700°C (holding time above 700°C).
- laser heating a fiber laser was used, and the focal spot diameter of the laser light in the rolling direction (i.e., the diameter including 86% of the laser output) was set to 30 ⁇ m (except for Tests No. 130 and No.
- the laser irradiation energy density, laser scanning speed, and shape of the laser irradiation area were varied in a composite manner to control the heating rate, maximum temperature, and holding time above 700°C.
- a person skilled in the art can combine the various conditions of the localized rapid heating method to control the desired heating rate, maximum temperature reached, and holding time above 700°C.
- test No. 128 the laser beam was elongated in the scanning direction, and the holding time from reaching the maximum temperature to cooling to 700 ° C. during local rapid heating was controlled to 0.2 seconds, so that coarse Goss orientation grains having an orientation close to the ideal Goss orientation were formed in the locally heated area.
- test No. 129 general laser irradiation conditions for magnetic domain refinement were applied.
- the focusing spot diameter was set to 0.5 mm
- the laser irradiation energy density was set to 2.0 J/mm 2
- the laser beam irradiation portion was controlled so that it would eventually become the grain boundary of the secondary recrystallized grain.
- the focusing spot diameter was set to 0.5 mm
- the laser irradiation energy density was set to 30.0 J/mm 2
- the laser beam irradiation portion was controlled so that it would eventually become the grain boundary of the secondary recrystallized grain.
- the local heating condition “Linear or spotted” indicates the shape of the localized heated area on the surface of the cold-rolled steel sheet
- the local heating conditions “Rolling direction spacing” and “Width direction spacing” indicate the spacing in the rolling direction and transverse direction at which the localized heated areas are arranged on the surface of the cold-rolled steel sheet.
- the localized heated areas are arranged at equal intervals in the rolling direction and transverse direction. Note that when providing localized heated areas on the surface of the cold-rolled steel sheet, they are arranged so that the distribution of the localized heated areas is not uneven.
- the widthwise spacing of the localized heating conditions for localized rapid heating, "end 10,” indicates that a localized heating area was formed only at a position 10 mm from the end of the steel plate in the direction perpendicular to the rolling direction.
- the cold-rolled steel sheets after the localized rapid heating were subjected to decarburization annealing under the conditions shown in Tables 3 to 10.
- the degree of oxidation (PH 2 O/PH 2 ) in the annealing atmosphere (furnace atmosphere) was set to 0.13.
- the decarburized annealed steel sheets produced were nitrided at 750°C in a nitrogen-hydrogen-ammonia atmosphere to set the nitrogen content of the steel sheets to 220 ppm.
- An annealing separator mainly composed of MgO was then applied, and finish annealing was performed.
- the steel sheet was heated to 1000°C at 15°C/hr (°C/hour) in a mixed atmosphere of hydrogen and nitrogen, and then heated to 1200°C at the heating rate shown in Tables 11 to 18.
- the temperature gradient shown in Tables 11 to 18 was applied in the direction perpendicular to the rolling C to the boundary between the primary recrystallization region and the secondary recrystallization region in the steel sheet.
- a temperature gradient of " ⁇ 1.0" in the heating process of the finish annealing indicates that the temperature gradient in the heating process was not substantially controlled.
- the steel sheet was held at 1200°C for 20 hr (hours) in a hydrogen atmosphere.
- the steel sheet After final annealing, the steel sheet is coated with an insulating coating solution made mainly of colloidal silica and phosphate, with chromic anhydride added as needed, and baked to form an insulating coating.
- an insulating coating solution made mainly of colloidal silica and phosphate, with chromic anhydride added as needed, and baked to form an insulating coating.
- the steel sheet on which the insulating coating was formed was irradiated with a laser in a linear manner so as to extend in a direction intersecting the rolling direction on the rolled surface of the steel sheet, with a rolling direction interval of 10 mm, an irradiation diameter of 300 ⁇ m, and with the energy density Ua shown in Tables 11 to 18.
- the energy density Ua of "untreated" indicates that laser irradiation for magnetic domain subdivision was not performed.
- grooves were formed in a linear manner so as to extend in a direction intersecting the rolling direction on the rolled surface of the steel sheet, with a rolling direction interval of 5 mm, an average groove width of 100 ⁇ m, and an average groove depth shown in Tables 11 to 18, on the steel sheet before the insulating coating was formed, and then the insulating coating was formed.
- the groove depth of "-" indicates that groove formation for magnetic domain subdivision was not performed.
- the grain-oriented electrical steel sheets according to the present invention had favorably controlled magnetic flux density B 8 , core loss W 17/50 , and magnetostriction rate level Lva200@1.7T.
- the grain-oriented electrical steel sheets which are comparative examples did not have the magnetic flux density B 8 , the core loss W 17/50 , or the magnetostriction rate level Lva200@1.7T controlled to a desired value.
- the above aspect of the present invention makes it possible to provide a grain-oriented electrical steel sheet that is excellent in magnetic flux density, core loss, and noise characteristics, even when magnetic domain control technology is applied, and therefore has high industrial applicability.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Electromagnetism (AREA)
- Manufacturing & Machinery (AREA)
- Dispersion Chemistry (AREA)
- Power Engineering (AREA)
- Manufacturing Of Steel Electrode Plates (AREA)
- Soft Magnetic Materials (AREA)
Abstract
Description
本願は、2023年6月29日に、日本に出願された特願2023-106861号に基づき優先権を主張し、その内容をここに援用する。
母材鋼板と絶縁被膜とを有し且つ磁区制御された方向性電磁鋼板であって、
800A/mで励磁したときの圧延方向の磁束密度を単位:TでB8と定義し、
周波数50Hzで磁束密度1.7Tに励磁したときの鉄損を単位:W/kgでW17/50と定義し、
周波数50Hzで磁束密度1.7Tに励磁したときの磁歪波形のうちの200Hz成分の磁歪量から求める磁歪速度レベルを単位:dBでLva200@1.7Tと定義したとき、
前記B8が、B8≧1.940を満たし、
前記W17/50が、W17/50≦0.670を満たし、
前記Lva200@1.7Tが、△Lva200@1.7T≦46.0を満たす。
母材鋼板と絶縁被膜とを有し、
800A/mで励磁したときの圧延方向の磁束密度を単位:TでB8と定義し、
周波数50Hzで磁束密度1.7Tに励磁したときの鉄損を単位:W/kgでW17/50と定義し、
周波数50Hzで磁束密度1.7Tに励磁したときの磁歪波形のうちの200Hz成分の磁歪量から求める磁歪速度レベルを単位:dBでLva200@1.7Tと定義したとき、
上記B8が、B8≧1.940を満たし、
上記W17/50が、W17/50≦0.670を満たし、
上記△Lva200@1.7Tが、Lva200@1.7T≦46.0を満たす。
ρ:空気の密度(kg/m3)
c:音速(m/秒)
P0:1kHzの音を人間が聞き取ることのできる最小の圧力(Pa)
fi:周波数(Hz)
λ(fi):フーリエ変換した周波数ごとの磁歪量
α(fi):周波数fiのA特性
π:円周率
ρ=1.185(kg/m3)
c=346.3(m/秒)
P0=2×10⁻⁵(Pa)
fi=200(Hz)
α(fi):JIS C 1509-1(2005)の表2に記載の値
Si:2.0~7.0%、
C:0~0.0050%、
Mn:0~1.0%、
S及びSe:合計で0~0.0150%、
Al:0~0.0650%、
N:0~0.0050%、
Nb、V、Mo、Ta、及びW:合計で0~0.050%、
Cu:0~0.40%、
Bi:0~0.010%、
B:0~0.080%、
P:0~0.50%、
Ti:0~0.0150%、
Sn:0~0.10%、
Sb:0~0.10%、
Cr:0~0.30%、
Ni:0~1.0%、
を含有し、残部がFeおよび不純物からなればよい。
Si(シリコン)は、母材鋼板にとって基本元素である。Si含有量が2.0%未満であると、渦電流損を十分に低減できないため、良好な磁気特性が得られない。そのため、母材鋼板のSi含有量は2.0%以上とする。Si含有量は、好ましくは2.50%以上、より好ましくは3.0%以上である。一方で、Si含有量が7.0%を超えると、鋼板が脆化し、製造に際して通板性が顕著に劣化するので、母材鋼板のSi含有量は7.0%以下とする。Si含有量は、好ましくは4.50%以下、より好ましくは4.0%以下である。
C(炭素)は、母材鋼板にとって選択元素である。Cは鋼片(スラブ)に含有されるが、仕上げ焼鈍後の母材鋼板にCが過剰に残留すると、良好な鉄損特性が得られないことがある。そのため、母材鋼板のC含有量は0.0050%以下であればよい。C含有量は、好ましくは0.0040%以下、より好ましくは0.0030%以下である。一方で、母材鋼板のC含有量の下限値は、特に制限されず、0%であればよい。ただ、C含有量を0%にすることは工業的に容易ではないので、C含有量を、0%超としてもよく、0.00010%以上としてもよい。
Mn(マンガン)は、母材鋼板にとって選択元素である。Mnは鋼片(スラブ)に含有されるが、過剰に含有されると、二次再結晶焼鈍時に鋼が相変態し、二次再結晶が十分に進行せず、良好な磁気特性が得られないことがある。そのため、母材鋼板のMn含有量は1.0%以下であればよい。Mn含有量は、好ましくは0.50%以下、より好ましくは0.20%以下である。一方で、母材鋼板のMn含有量の下限値は、特に制限されず、0%であればよい。ただ、Mnは、MnSやMnSeを形成して二次再結晶時のインヒビターとしての効果を有するので、Mn含有量を、0%超としてもよく、0.00010%以上としてもよい。
S(硫黄)及びSe(セレン)は、母材鋼板にとって選択元素である。S及びSeは鋼片(スラブ)に含有されるが、仕上げ焼鈍後の母材鋼板にS及びSeが過剰に残留すると、磁気特性に悪影響を及ぼすことがある。そのため、母材鋼板のS及びSeの合計含有量は0.0150%以下であればよい。S及びSeの合計含有量は、好ましくは0.010%以下、より好ましくは0.0050%以下である。一方で、母材鋼板のS及びSeの合計含有量の下限値は、特に制限されず、0%であればよい。ただ、S及びSeは、MnSやMnSeを形成して二次再結晶時のインヒビターとしての効果を有するので、S及びSeの合計含有量を、0%超としてもよく、0.00010%以上としてもよい。
Al(アルミニウム)は、母材鋼板にとって選択元素である。Alは鋼片(スラブ)に含有されるが、仕上げ焼鈍後の母材鋼板にAlが過剰に残留すると、磁気特性に悪影響を及ぼすことがある。そのため、母材鋼板のAl含有量は0.0650%以下であればよい。Al含有量は、好ましくは0.040%以下、より好ましくは0.035%以下である。一方で、母材鋼板のAl含有量の下限値は、特に制限されず、0%であればよい。ただ、Alは、AlNを形成して二次再結晶時のインヒビターとしての効果を有するので、Al含有量を、0%超としてもよく、0.00010%以上としてもよい。なお、上記のAl含有量は、酸可溶性Al(sol.Al)である。
N(窒素)は、母材鋼板にとって選択元素である。Nは鋼片(スラブ)に含有されるが、仕上げ焼鈍後の母材鋼板にNが過剰に残留すると、磁気特性に悪影響を及ぼすことがある。そのため、母材鋼板のN含有量は0.0050%以下であればよい。N含有量は、好ましくは0.0040%以下、より好ましくは0.0030%以下である。一方で、母材鋼板のN含有量の下限値は、特に制限されず、0%であればよい。ただ、Nは、AlNを形成して二次再結晶時のインヒビターとしての効果を有するので、N含有量を、0%超としてもよく、0.00010%以上としてもよい。
Nb(ニオブ)、V(バナジウム)、Mo(モリブデン)、Ta(タンタル)、W(タングステン)は、母材鋼板にとって選択元素である。母材鋼板にNb群元素(Nb、V、Mo、Ta、及びWの1種以上)が過剰に残留すると、磁気特性に悪影響を及ぼすことがある。そのため、母材鋼板のNb、V、Mo、Ta、及びWの合計含有量は、0.050%以下であればよい。Nb群元素は、好ましくは0.030%以下、好ましくは0.020%以下、より好ましくは0.010%以下である。一方で、母材鋼板のNb、V、Mo、Ta、及びWの合計含有量は、特に制限されず、0%であればよい。ただ、Nb、V、Mo、Ta、またはWは、炭化物や窒化物や炭窒化物を形成して二次再結晶時のインヒビターとしての効果を有するので、Nb、V、Mo、Ta、及びWの合計含有量を、0%超としてもよく、0.003%以上としてもよい。
Cu(銅)は、母材鋼板にとって選択元素である。Cu含有量が0.40%を超えると、熱間圧延中、鋼板が脆化することがある。そのため、母材鋼板のCu含有量は0.40%以下であればよい。Cu含有量は、好ましくは0.30%以下、より好ましくは0.10%以下である。一方で、Cu含有量の下限値は、特に制限されず、0%であればよい。ただ、Cuは、Goss方位の集積度を高めて、磁気特性を改善させる効果を有するので、Cu含有量は、0%超としてもよく、0.010%以上としてもよい。
Bi(ビスマス)は、母材鋼板にとって選択元素である。Bi含有量が0.010%を超えると、被膜密着性が低下することがある。また、仕上げ焼鈍時の純化が不十分でBiが過剰に残留すると、磁気特性に悪影響を及ぼすことがある。そのため、母材鋼板のBi含有量は0.010%以下であればよい。Bi含有量は、好ましくは0.0050%以下、より好ましくは0.0020%以下、より好ましくは0.0010%以下である。一方で、Bi含有量の下限値は、特に制限されず、0%であればよい。ただ、Biは、磁束密度を向上させる効果を有するので、Bi含有量は、0%超としてもよく、0.00050%以上としてもよい。
B(ボロン)は、母材鋼板にとって選択元素である。B含有量が0.080%を超えると、磁束密度のばらつき(標準偏差)が大きくなることがある。そのため、B含有量は0.080%以下であればよい。Bi含有量は、好ましくは0.070%以下、より好ましくは0.060%以下である。一方で、B含有量の下限値は、特に制限されず、0%であればよい。ただ、Bは、窒化物を形成して二次再結晶時のインヒビターとしての効果を有するので、B含有量は、0%超としてもよく、0.00050%以上としてもよい。
P(燐)は、母材鋼板にとって選択元素である。P含有量が0.50%を超えれば、鋼板の加工性が顕著に低下することがある。そのため、母材鋼板のP含有量は0.50%以下であればよい。P含有量は、好ましくは0.30%以下、より好ましくは0.10%以下である。一方で、P含有量の下限値は、特に制限されず、0%であればよい。ただ、Pは、集合組織を改善し、鋼板の磁気特性を改善する効果を有するので、P含有量を、0%超としてもよく、0.0020%以上としてもよい。
Ti(チタン)は、母材鋼板にとって選択元素である。Ti含有量が0.0150%を超えれば、磁気特性がに低下することがある。そのため、母材鋼板のTi含有量は0.0150%以下であればよい。Ti含有量は、好ましくは0.0130%以下、より好ましくは0.010%以下である。一方で、Ti含有量の下限値は、特に制限されず、0%であればよい。ただ、Tiは、炭化物や窒化物や炭窒化物を形成して二次再結晶時のインヒビターとしての効果を有するので、Ti含有量を、0%超としてもよく、0.0020%以上としてもよい。
Sn(スズ)は、母材鋼板にとって選択元素である。Sn含有量が0.10%を超えると、二次再結晶が不安定となり、磁気特性に悪影響を及ぼすことがある。そのため、母材鋼板のSn含有量は0.10%以下であればよい。Sn含有量は、好ましくは0.090%以下、より好ましくは0.080%以下である。一方で、Sn含有量の下限値は、特に制限されず、0%であればよい。ただ、Snは、Goss方位の集積度を高めて、磁気特性を改善させる効果を有するので、Sn含有量は、0%超としてもよく、0.0050%以上としてもよい。
Sb(アンチモン)は、母材鋼板にとって選択元素である。Sb含有量が0.10%を超えると、磁気特性に悪影響を及ぼすことがある。そのため、母材鋼板のSb含有量は0.10%以下であればよい。Sb含有量は、好ましくは0.090%以下、より好ましくは0.080%以下である。一方で、Sb含有量の下限値は、特に制限されず、0%であればよい。ただ、Sbは、インヒビターとして機能して二次再結晶を安定化する効果を有するので、Sb含有量は、0%超としてもよく、0.010%以上としてもよい。
Cr(クロム)は、母材鋼板にとって選択元素である。Cr含有量が0.30%を超えると、Cr酸化物を形成し、磁気特性に悪影響を及ぼすことがある。そのため、母材鋼板のCr含有量は0.30%以下であればよい。Cr含有量は、好ましくは0.20%以下、より好ましくは0.10%以下である。一方で、Cr含有量の下限値は、特に制限されず、0%であればよい。ただ、Crは、Goss方位の集積度を高めて、磁気特性を改善させる効果を有するので、Cr含有量は、0%超としてもよく、0.010%以上としてもよい。
Ni(ニッケル)は、母材鋼板にとって選択元素である。Ni含有量が1.0%を超えると、二次再結晶が不安定になることがある。そのため、母材鋼板のNi含有量は1.0%以下であればよい。Ni含有量は、好ましくは0.20%以下、より好ましくは0.10%以下である。一方で、Ni含有量の下限値は、特に制限されず、0%であればよい。ただ、Niは、電気抵抗を高めて鉄損を低減する効果を有するので、Ni含有量は、0%超としてもよく、0.010%以上としてもよい。
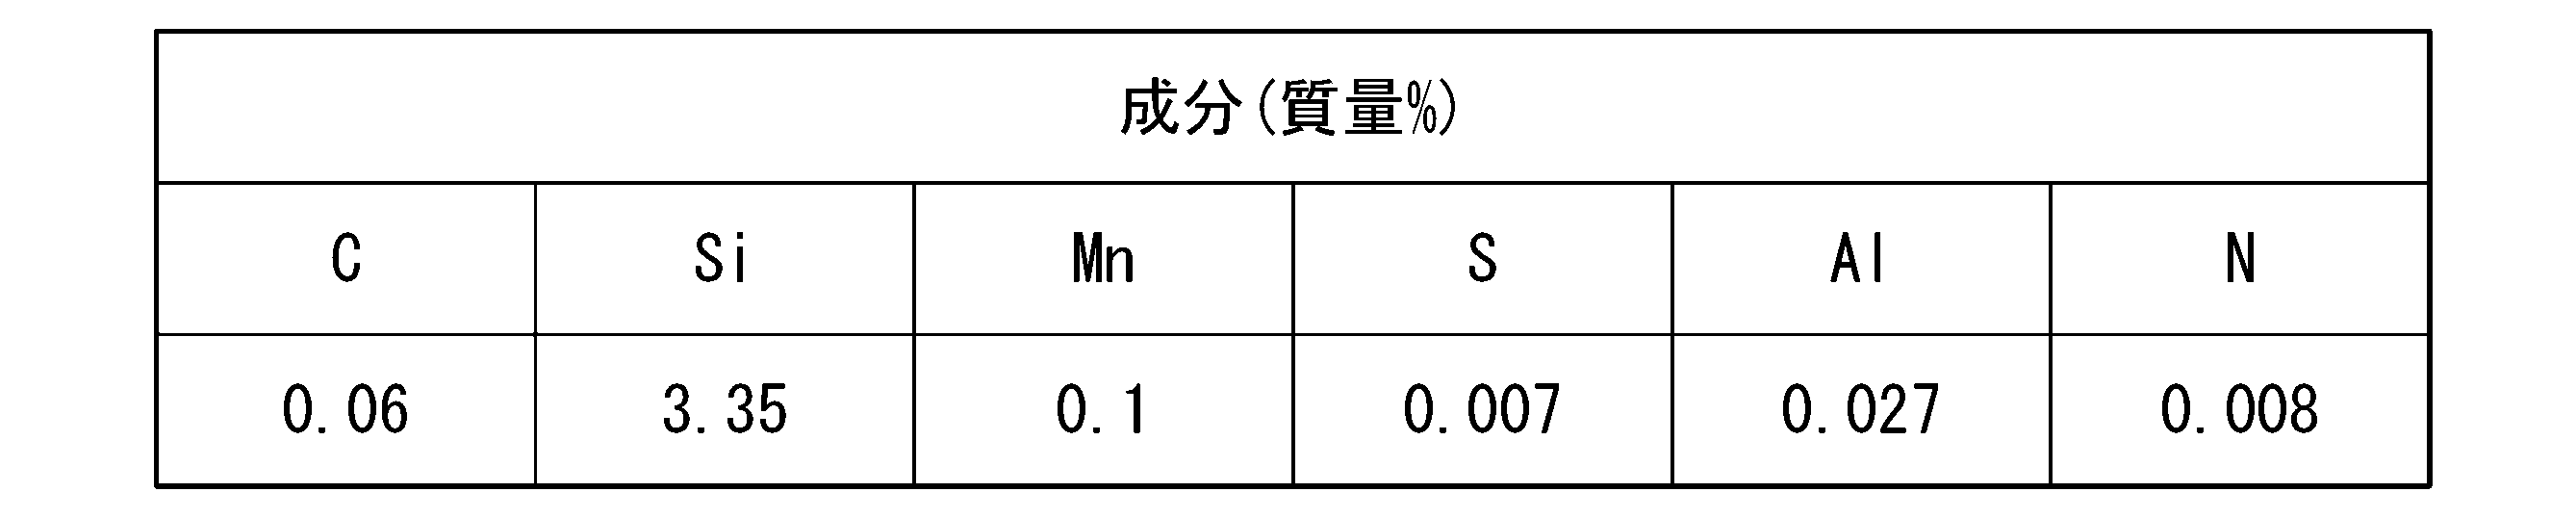
鋳造工程では、スラブを準備する。スラブの製造方法の一例は次のとおりである。溶鋼を製造(溶製)する。溶鋼を用いてスラブを製造する。連続鋳造法によりスラブを製造してもよい。溶鋼を用いてインゴットを製造し、インゴットを分塊圧延してスラブを製造してもよい。スラブの厚さは、特に限定されない。スラブの厚さは、たとえば、150~350mmである。スラブの厚さは、好ましくは、220~280mmである。スラブとして、厚さが10~70mmの、いわゆる薄スラブを用いてもよい。薄スラブを用いる場合、熱間圧延工程において、仕上げ圧延前の粗圧延を省略できる。
炭素(C)は、製造工程においては一次再結晶組織の制御に有効な元素であるものの、最終製品への含有量が過剰であると磁気特性に悪影響を及ぼす。したがって、C含有量は0.085%以下である。C含有量の好ましい上限は0.075%である。Cは脱炭焼鈍工程及び仕上げ焼鈍工程で純化され、0.005%以下となる。Cを含む場合、工業生産における生産性を考慮すると、C含有量の下限は0%超であってもよく、0.001%であってもよい。
シリコン(Si)は、方向性電磁鋼板の電気抵抗を高めて鉄損を低下させる。Si含有量が2.0%未満であれば、仕上げ焼鈍時にγ変態が生じて、方向性電磁鋼板の結晶方位が損なわれてしまう。一方、Si含有量が7.0%を超えれば、冷間加工性が低下して、冷間圧延時に割れが発生しやすくなる。Si含有量の好ましい下限は2.5%であり、さらに好ましくは3.0%である。Si含有量の好ましい上限は4.5%であり、さらに好ましくは4.0%である。
マンガン(Mn)はS又はSeと結合して、MnS、又は、MnSeを生成し、インヒビターとして機能する。Mnを含有させる場合、Mn含有量が0.05~1.00%の範囲内にある場合に、二次再結晶が安定する。なお、インヒビターの機能の一部をNb群元素の窒化物によって担うことが可能である。この場合は、一般的なインヒビターとしてのMnS、又は、MnSe強度は弱めに制御する。このため、Mn含有量の好ましい上限は0.50%であり、さらに好ましくは0.20%である。
硫黄(S)及びセレン(Se)は、Mnと結合して、MnS又はMnSeを生成し、インヒビターとして機能する。S及びSeの少なくとも一方を含有させる場合、S及びSeの含有量が合計で0.003~0.035%であれば、二次再結晶が安定する。なお、インヒビターの機能の一部をNb群元素の窒化物によって担うことが可能である。この場合は、一般的なインヒビターとしてのMnS、又は、MnSe強度は弱めに制御する。このため、S及びSe含有量の合計の好ましい上限は0.025%であり、さらに好ましくは0.010%である。S及びSeは仕上げ焼鈍後に残留すると化合物を形成し、鉄損を劣化させる。そのため、仕上げ焼鈍中の純化により、S及びSeをできるだけ少なくすることが好ましい。
アルミニウム(Al)は、Nと結合して(Al、Si)Nとして析出し、インヒビターとして機能する。Alを含有させる場合、Al含有量が0.010~0.065%の範囲内にある場合に、後述の窒化により形成されるインヒビターとしてのAlNは二次再結晶温度域を拡大し、特に高温域での二次再結晶が安定する。したがって、Al含有量は0.010~0.065%である。Al含有量の好ましい下限は0.020%であり、さらに好ましくは0.025%である。二次再結晶の安定性の観点から、Al含有量の好ましい上限は0.040%であり、さらに好ましくは0.035%である。
窒素(N)は、Alと結合してインヒビターとして機能する。Nは製造工程の途中で窒化により含有させることが可能であるため下限は規定しない。例えば、N含有量の下限は0%超であってもよく、0.001%であってもよい。一方、Nを含有させる場合、N含有量が0.012%を超えれば、鋼板中に欠陥の一種であるブリスタが発生しやすくなる。N含有量の好ましい上限は0.010%であり、さらに好ましくは0.009%である。Nは仕上げ焼鈍工程で純化され、仕上げ焼鈍工程後には0.005%以下となる。
Nb群元素(Nb、V、Mo、Ta、及びWの1種以上)の合計含有量は0.050%以下であればよい。Nb群元素をインヒビターの一部として活用する場合、Nb群元素の合計含有量が0.030%以下であると、適切なタイミングで二次再結晶を開始させるので好ましい。また、発生する二次再結晶粒の方位が非常に好ましいものとなり、最終的に磁気特性にとって好ましい組織に制御できる。特に、Nb及びTaはその効果が強く好ましい。Nb群元素の合計含有量は下限値を設ける必要がなく、下限値が0%でもよい。この下限値は、0.003%であることが好ましい。
Cu:0.40%以下、
Bi:0.010%以下、
B:0.080%以下、
P:0.50%以下、
Ti:0.015%以下、
Sn:0.10%以下、
Sb:0.10%以下、
Cr:0.30%以下、
Ni:1.00%以下
の少なくとも1種を含有してもよい。
これら任意元素は、公知の目的に応じて含有させればよいため、任意元素の含有量の下限値を設ける必要はなく、下限値が0%でもよい。
熱間圧延工程は、所定の温度(例えば1100~1400℃)に加熱されたスラブの熱間圧延を行い、熱延鋼板を得る工程である。熱間圧延工程では、例えば、加熱工程で加熱された珪素鋼素材(スラブ)の粗圧延を行った後、仕上げ圧延を行って所定厚さ、例えば、1.8~3.5mmの熱延鋼板とする。仕上げ圧延終了後、熱延鋼板を所定の温度で巻き取る。
熱延板焼鈍工程は、熱間圧延工程で得た熱延鋼板を所定の温度条件(例えば750~1200℃で30秒間~10分間)で焼鈍して、焼鈍鋼板を得る工程である。熱延板焼鈍は、一般的に、熱間圧延工程後の熱延鋼板を焼鈍することにより、再結晶率や残存歪や結晶粒径などの鋼板組織を制御し、また鋼中の析出物形態を好ましく調整するために実施される。例えば、高温スラブ加熱プロセスにおいては、AlNなどの析出物の形態を最終的に制御する工程であり、均一かつ微細に析出するように条件調整する。熱延板焼鈍として、例えば、鋼板を1050℃~1150℃に加熱した後、AlNなどを適正に析出させるため、50~150秒かけて中間温度(850℃~950℃)まで緩冷却した後、水冷却してもよい。
冷間圧延工程は、熱延板焼鈍工程で得た焼鈍鋼板を、1回の冷間圧延、又は焼鈍(中間焼鈍)を介して複数回(2回以上)の冷間圧延(例えば総冷延率で80~95%)により、例えば、0.10~0.50mmの厚さを有する冷延鋼板を得る工程である。磁気特性を改善するために、例えば、冷間圧延のパス間温度を100℃~300℃程度にしてもよい。
本実施形態では、冷間圧延工程後の冷延鋼板に対して、局所加熱領域を形成するための局所急速加熱を行う。急速加熱方法としては、鋼板を局所的に加熱できるものであればよく、特に限定しない。例えば、鋼板の表裏面にスポット電極を接触させて鋼板内に電流を通電して加熱する方法、レーザー光や電子ビームなどを鋼板表面に照射して加熱する方法、誘導加熱によって局所的に加熱する方法、熱片を接触させて加熱する方法などを採用することができる。個々の局所加熱領域の大きさとしては、直径が10μm~10mm程度の点状領域、あるいは幅が10μm~10mm程度の線状領域とすることができる。また、通電加熱に用いる電極は、上記のように円形状の電極としてもよく、または線状の電極としてもよい。
脱炭焼鈍工程では、局所急速加熱工程後の冷延鋼板に対して、脱炭焼鈍(一次焼鈍)を行う。この脱炭焼鈍により、局所加熱影響領域に形成されるゴス方位粒の存在頻度が増大し、ゴス方位粒の粒径が増大し、理想ゴス方位に近い方位を持つ粗大ゴス方位粒が好ましく形成される。脱炭焼鈍条件としては、加熱速度を10~10000℃/秒、焼鈍温度を700~900℃、焼鈍時間を10~600秒とすればよい。また、冷延鋼板に脱炭焼鈍を行うことで、冷延鋼板中に含まれるCが除去される。脱炭焼鈍は、冷延鋼板中に含まれる「C」を除去するために、湿潤雰囲気中で行うことが好ましい。
窒化処理は、スラブ加熱温度が1280℃以下の低温スラブ加熱プロセスで有効な処理であり、二次再結晶におけるインヒビターの強度を調整するために重要な工程である。窒化処理は、脱炭処理の開始から、仕上げ焼鈍における二次再結晶の開始までの間に、鋼板の窒素量を40~200ppm程度増加させる。窒化処理としては、例えば、アンモニア等の窒化能のあるガスを含有する雰囲気中で焼鈍する処理、MnN等の窒化能を有する粉末を含む焼鈍分離剤を塗布した脱炭焼鈍鋼板を仕上げ焼鈍する処理等が例示される。窒化処理後の窒化量は130~350ppmとすることが好ましく、さらには150~250ppmとすることが好ましい。
焼鈍分離剤塗布工程は、脱炭焼鈍鋼板に焼鈍分離剤を塗布する工程である。焼鈍分離剤としては、例えば、MgOを主成分とする焼鈍分離剤やAl2O3を主成分とする焼鈍分離剤を用いることができる。焼鈍分離剤を塗布後の脱炭焼鈍鋼板は、コイル状に巻取った状態で、次の仕上げ焼鈍工程で仕上げ焼鈍される。
仕上げ焼鈍工程は、焼鈍分離剤が塗布された脱炭焼鈍鋼板に仕上げ焼鈍(二次焼鈍)を施し、二次再結晶を生じさせる工程である。この工程は、一次再結晶粒の成長をインヒビターにより抑制した状態で二次再結晶を進行させることによって、{100}<001>方位粒を優先成長させ、磁束密度を飛躍的に向上させる。
仕上げ焼鈍後の鋼板に、りん酸あるいはりん酸塩、無水クロム酸あるいはクロム酸塩およびコロイド状シリカを含むコーティング溶液を塗布して焼き付けて(例えば、350℃~1150℃で5~300秒間)、絶縁被膜を形成する。
絶縁被膜形成工程後の鋼板に、レーザー、プラズマ、機械的方法、エッチングなど、公知の手法により、局所的な微小歪領域または局所的な溝を形成する。
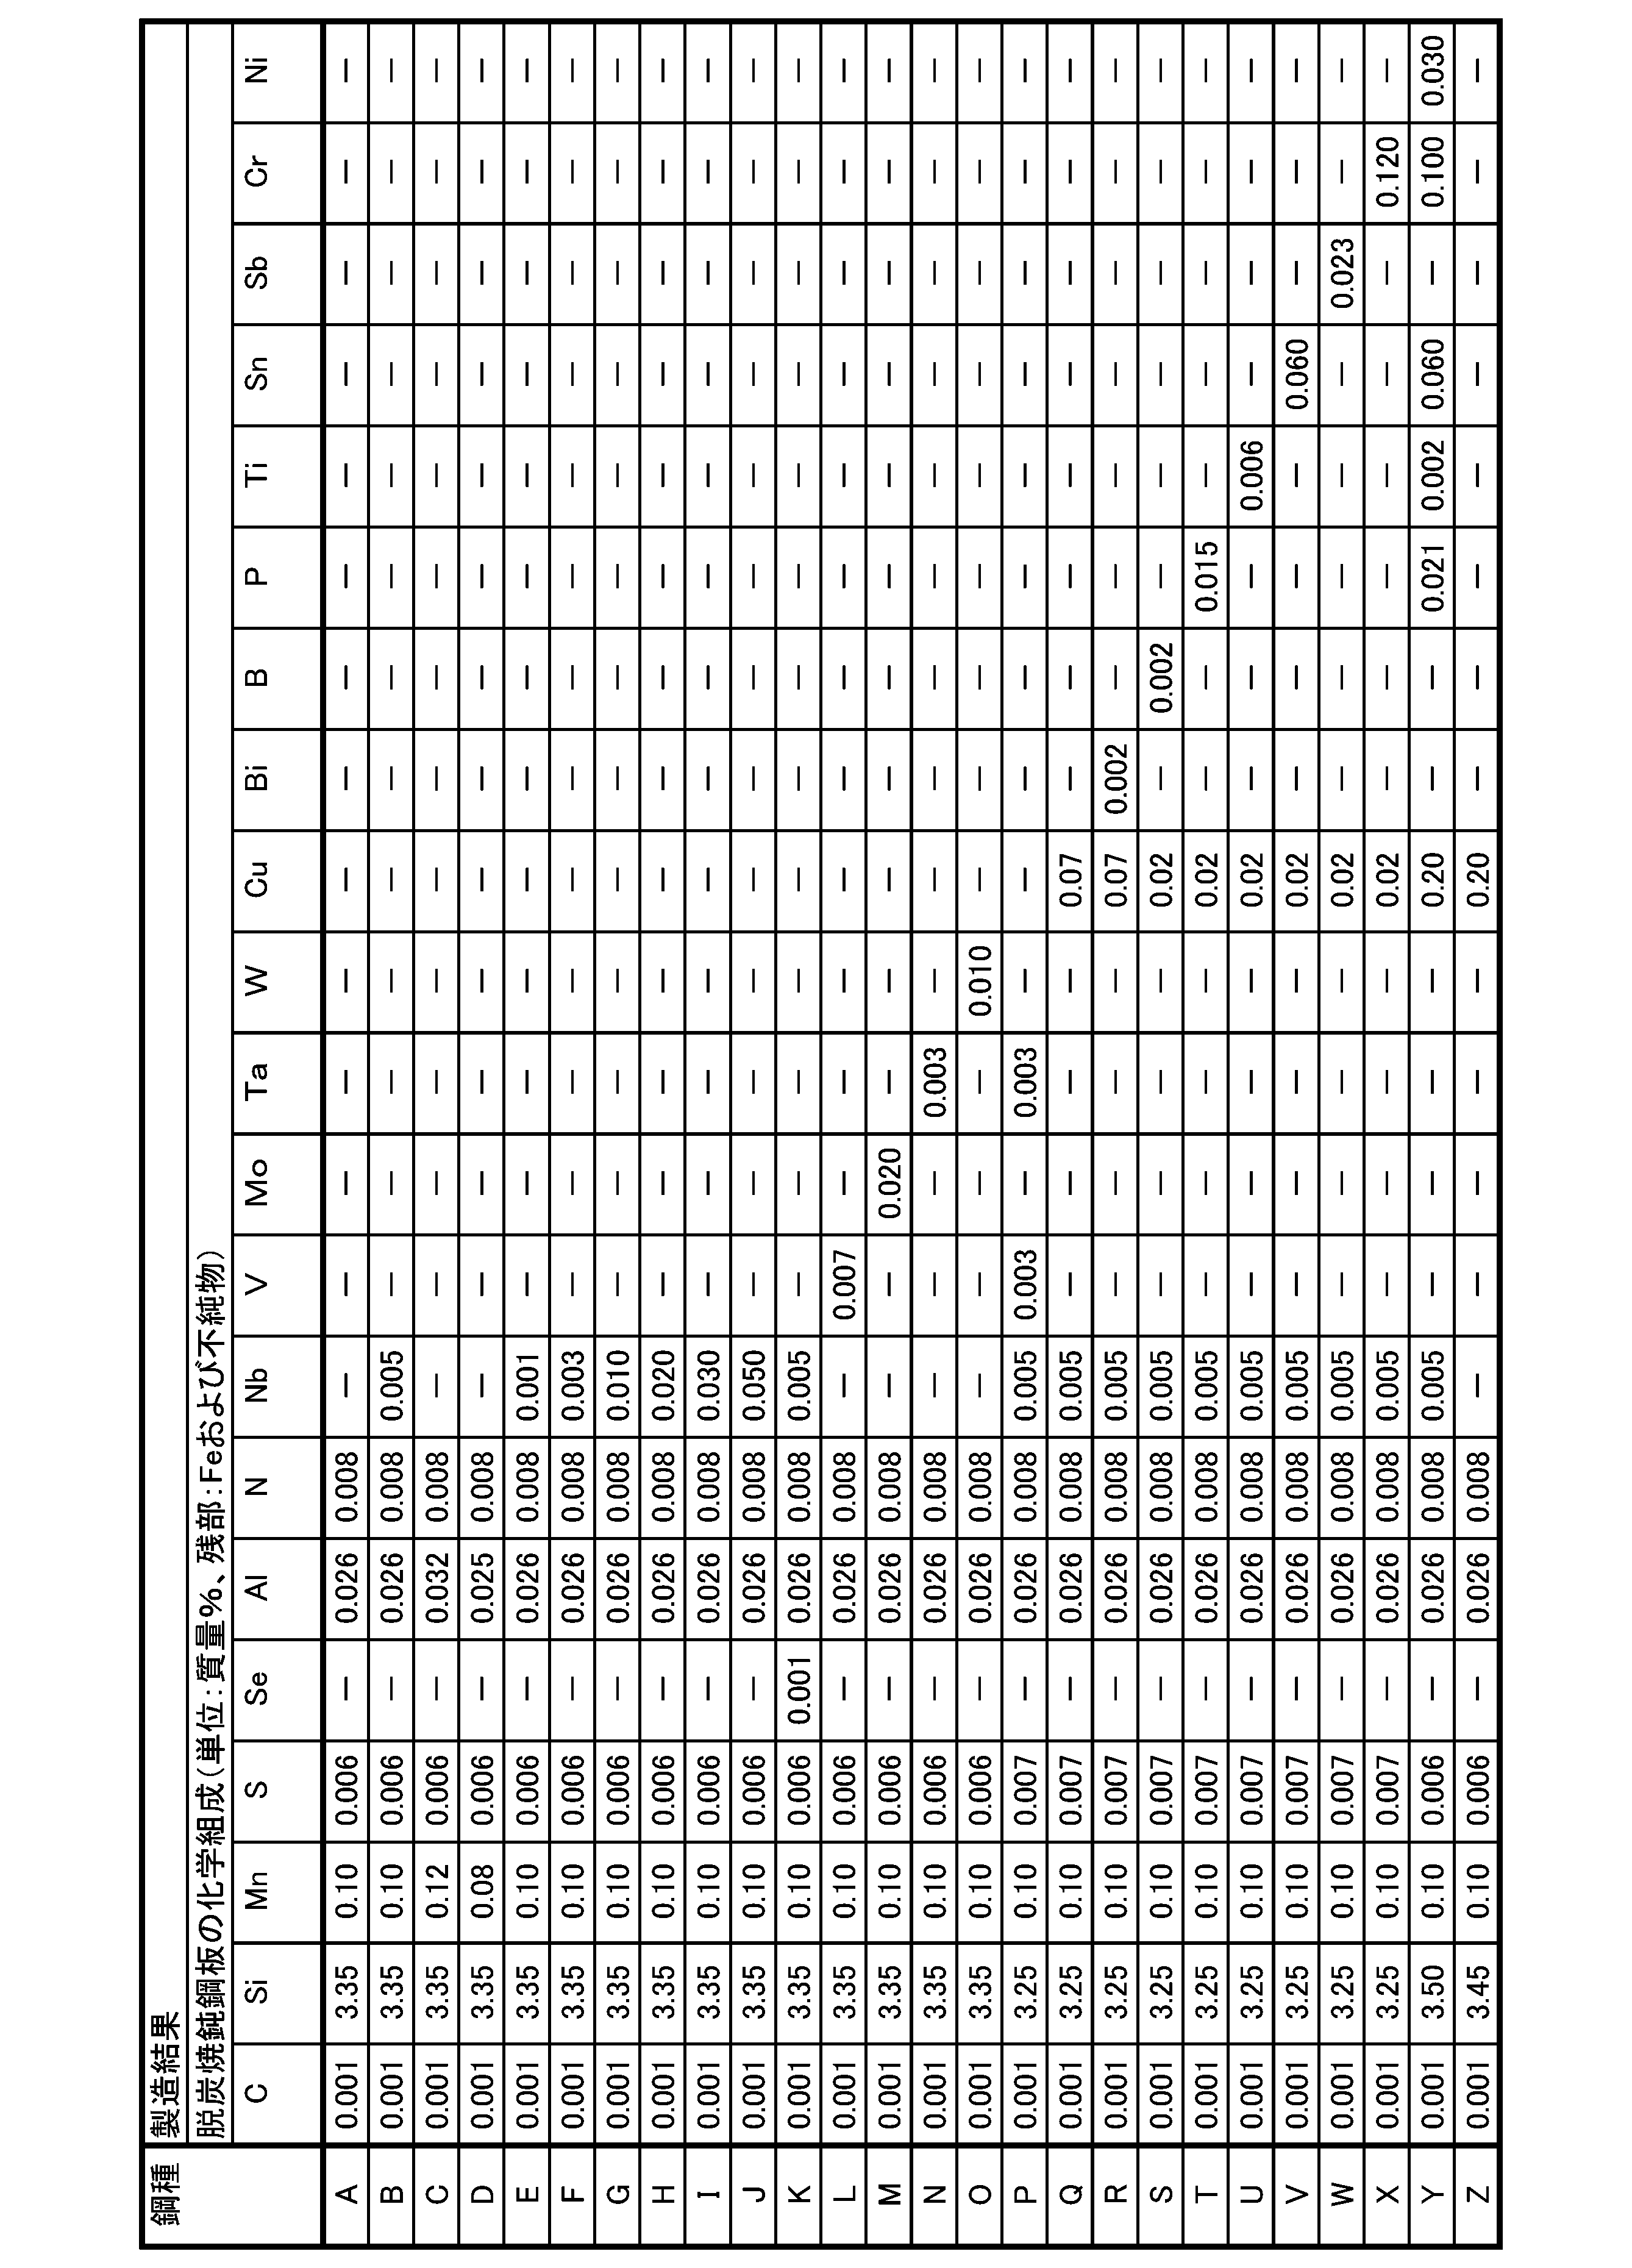
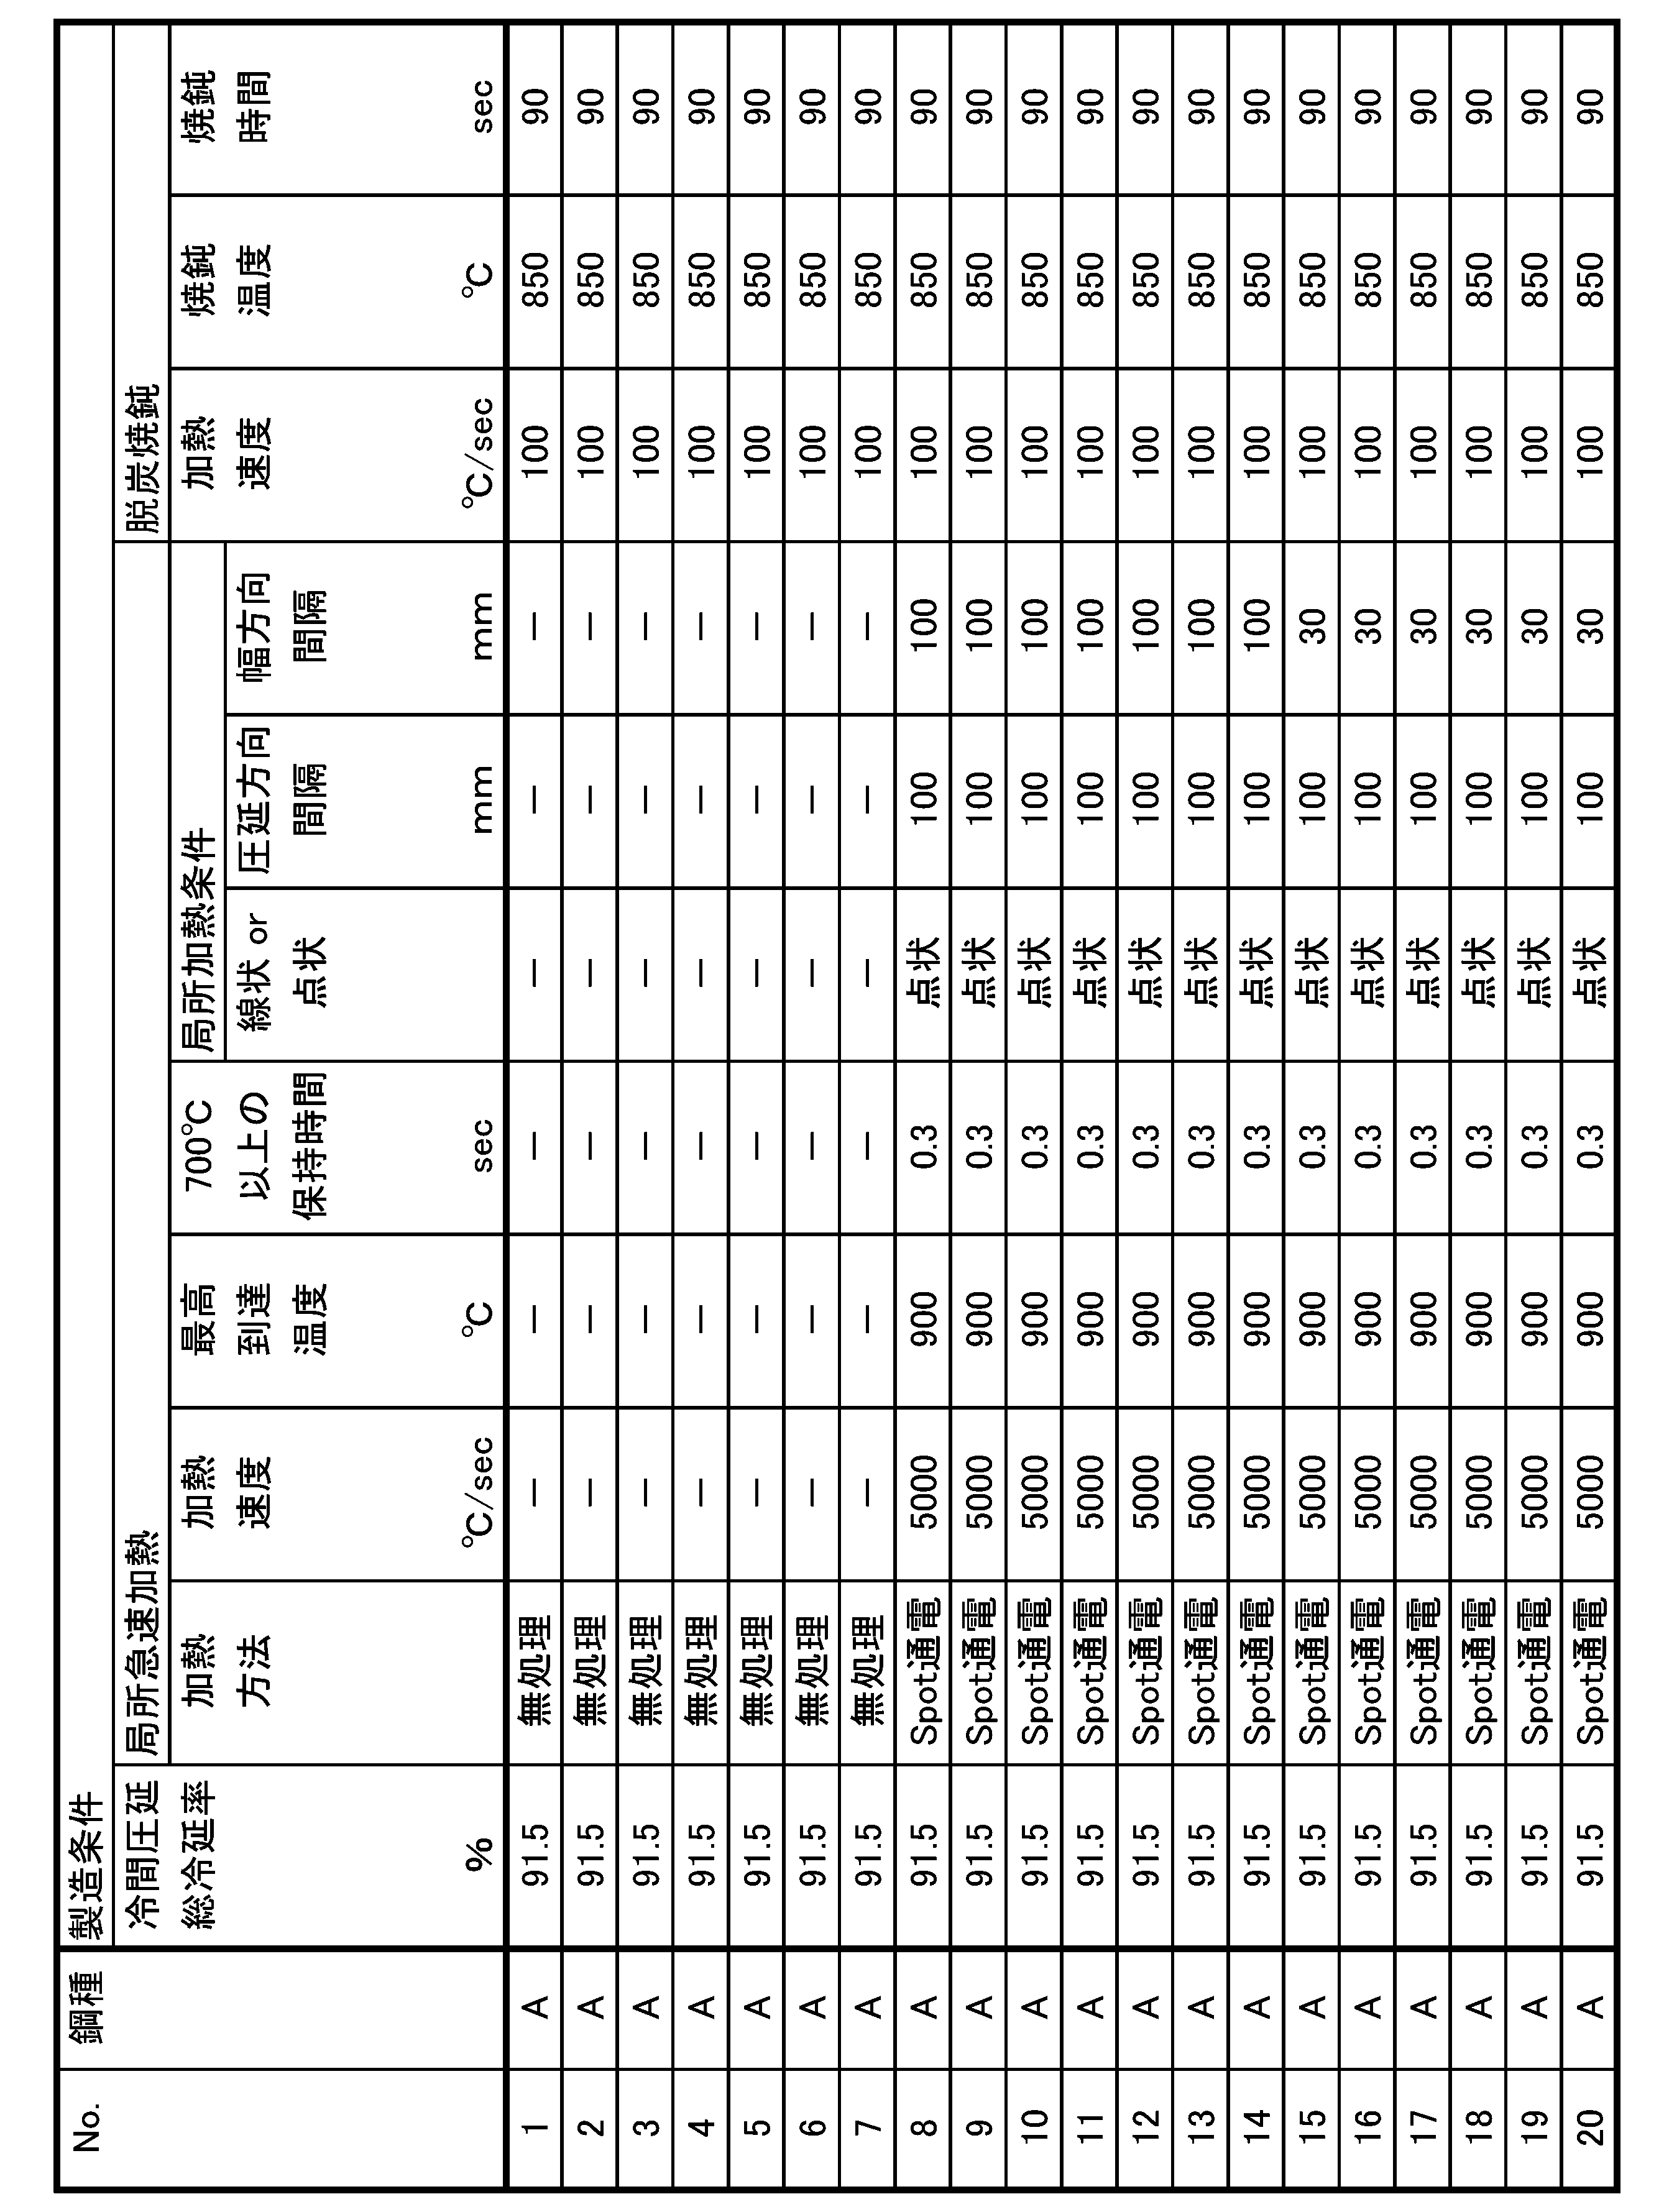
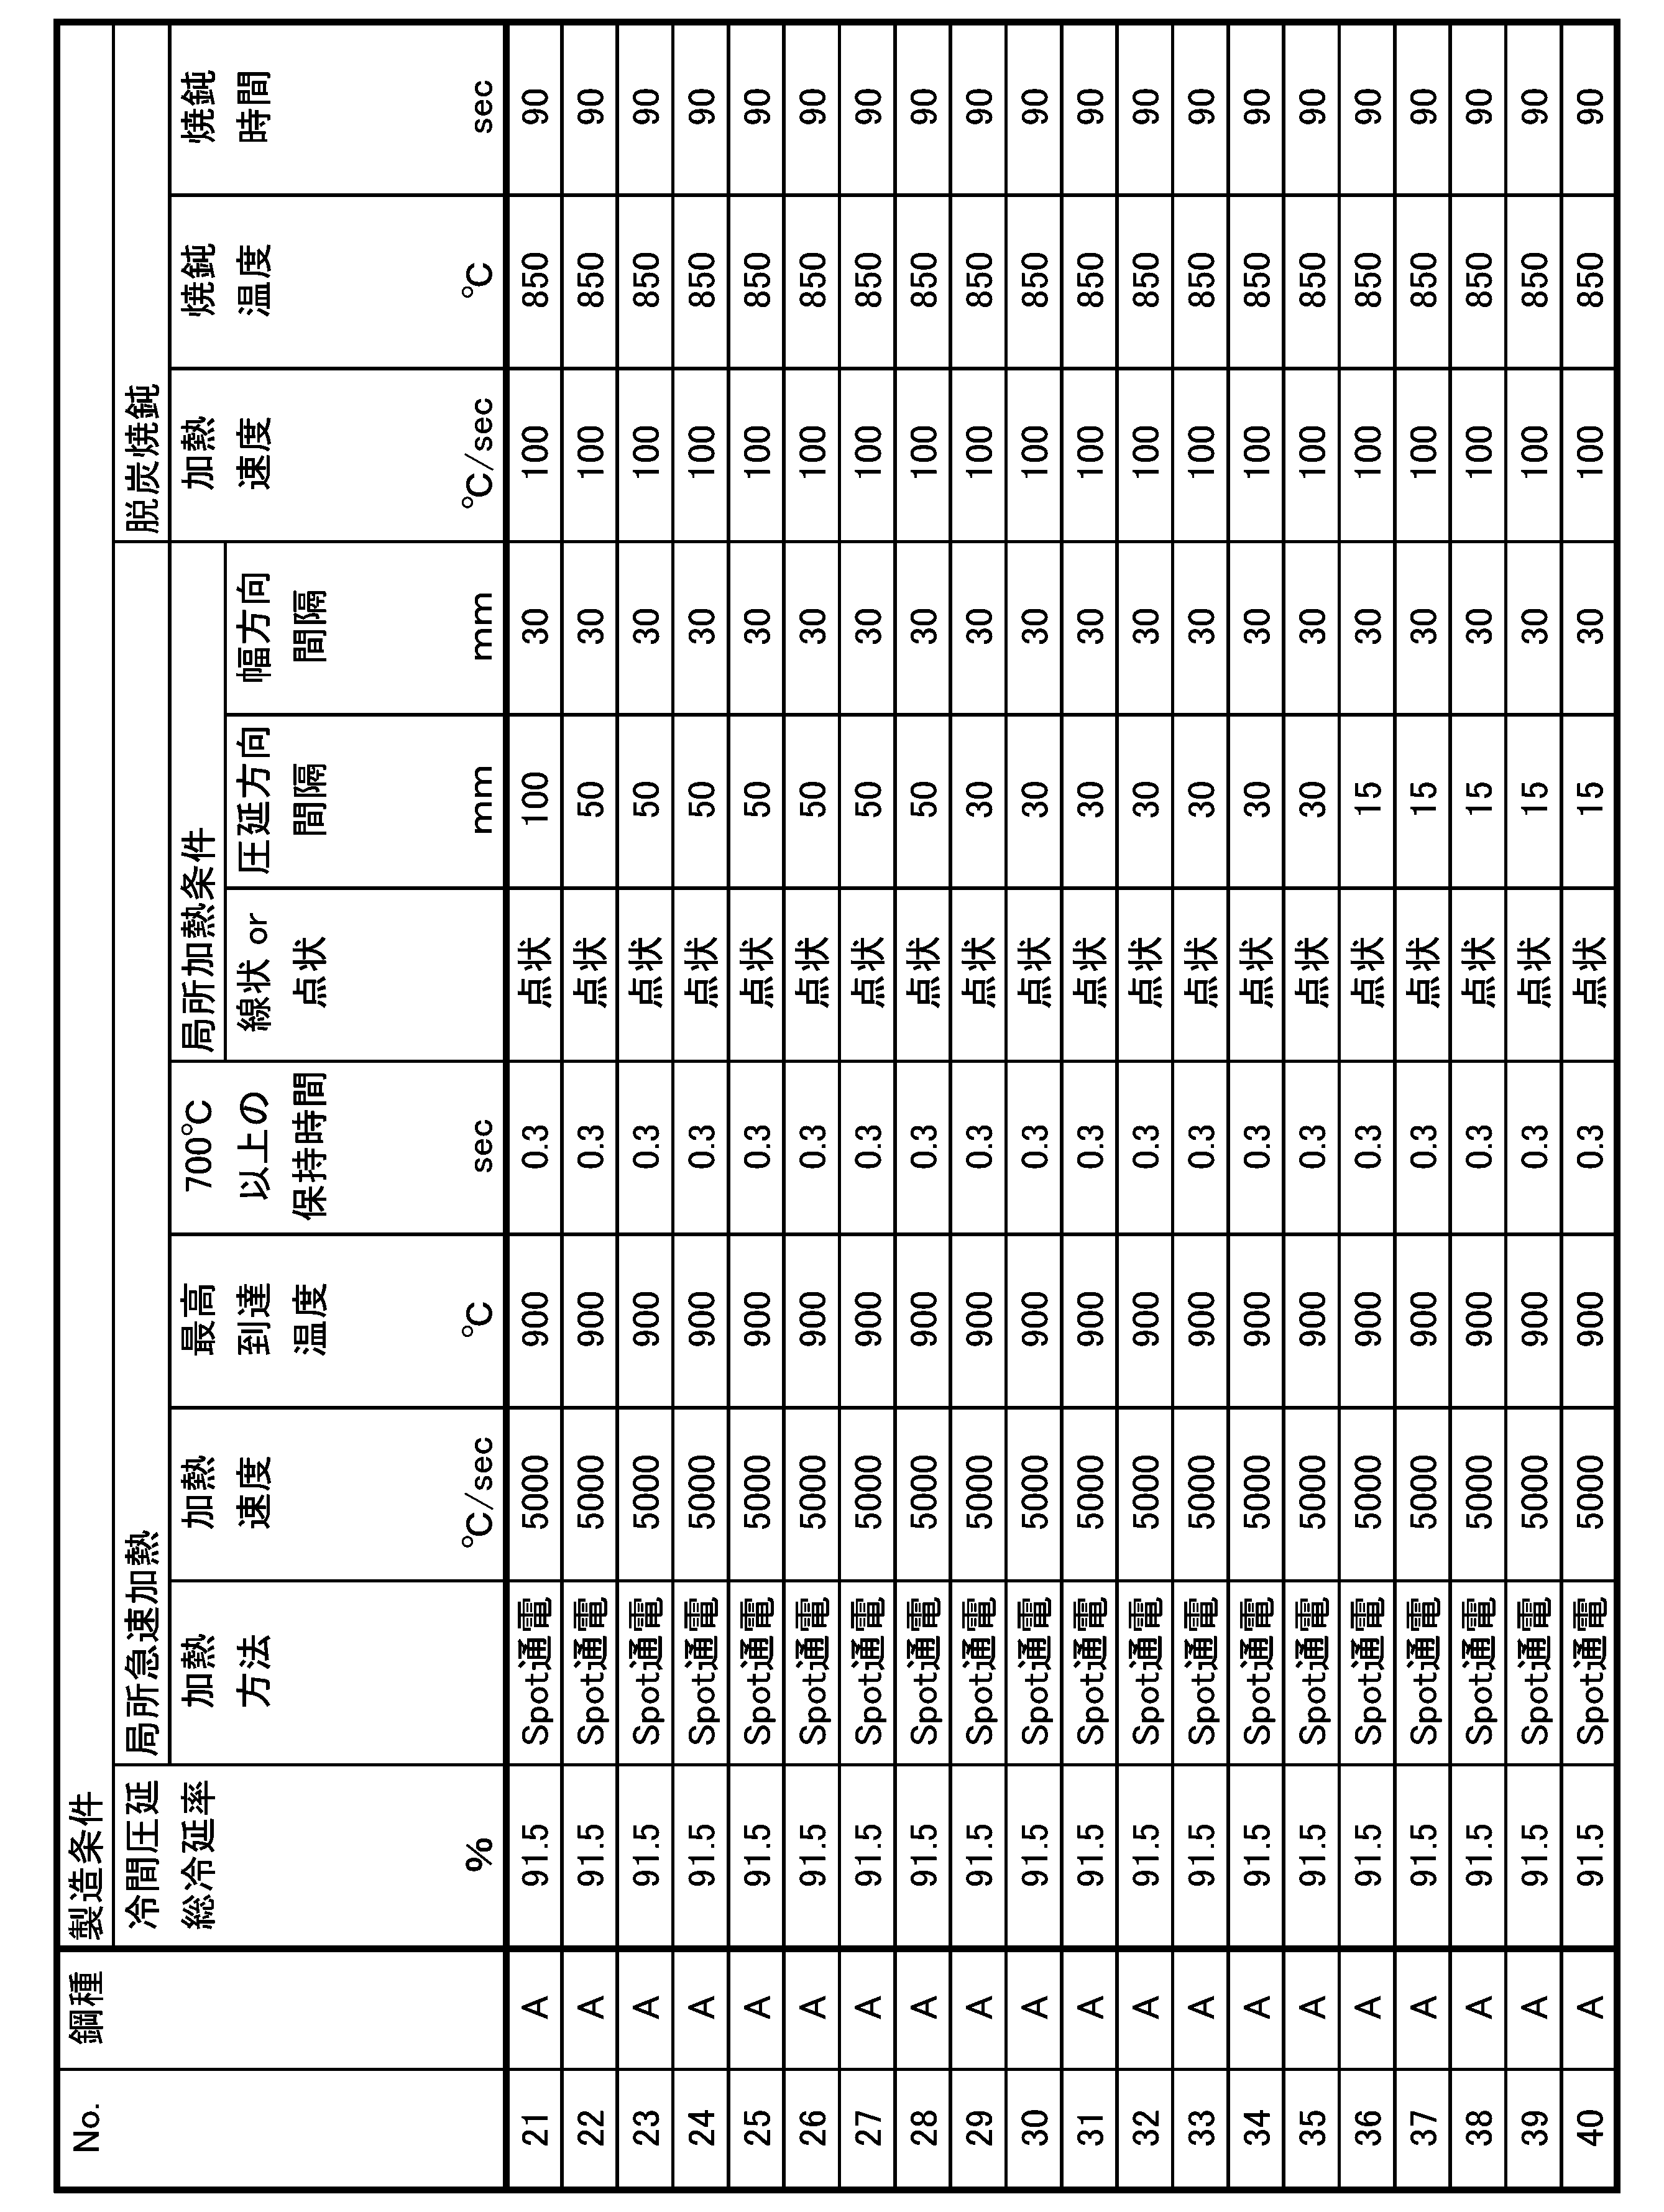
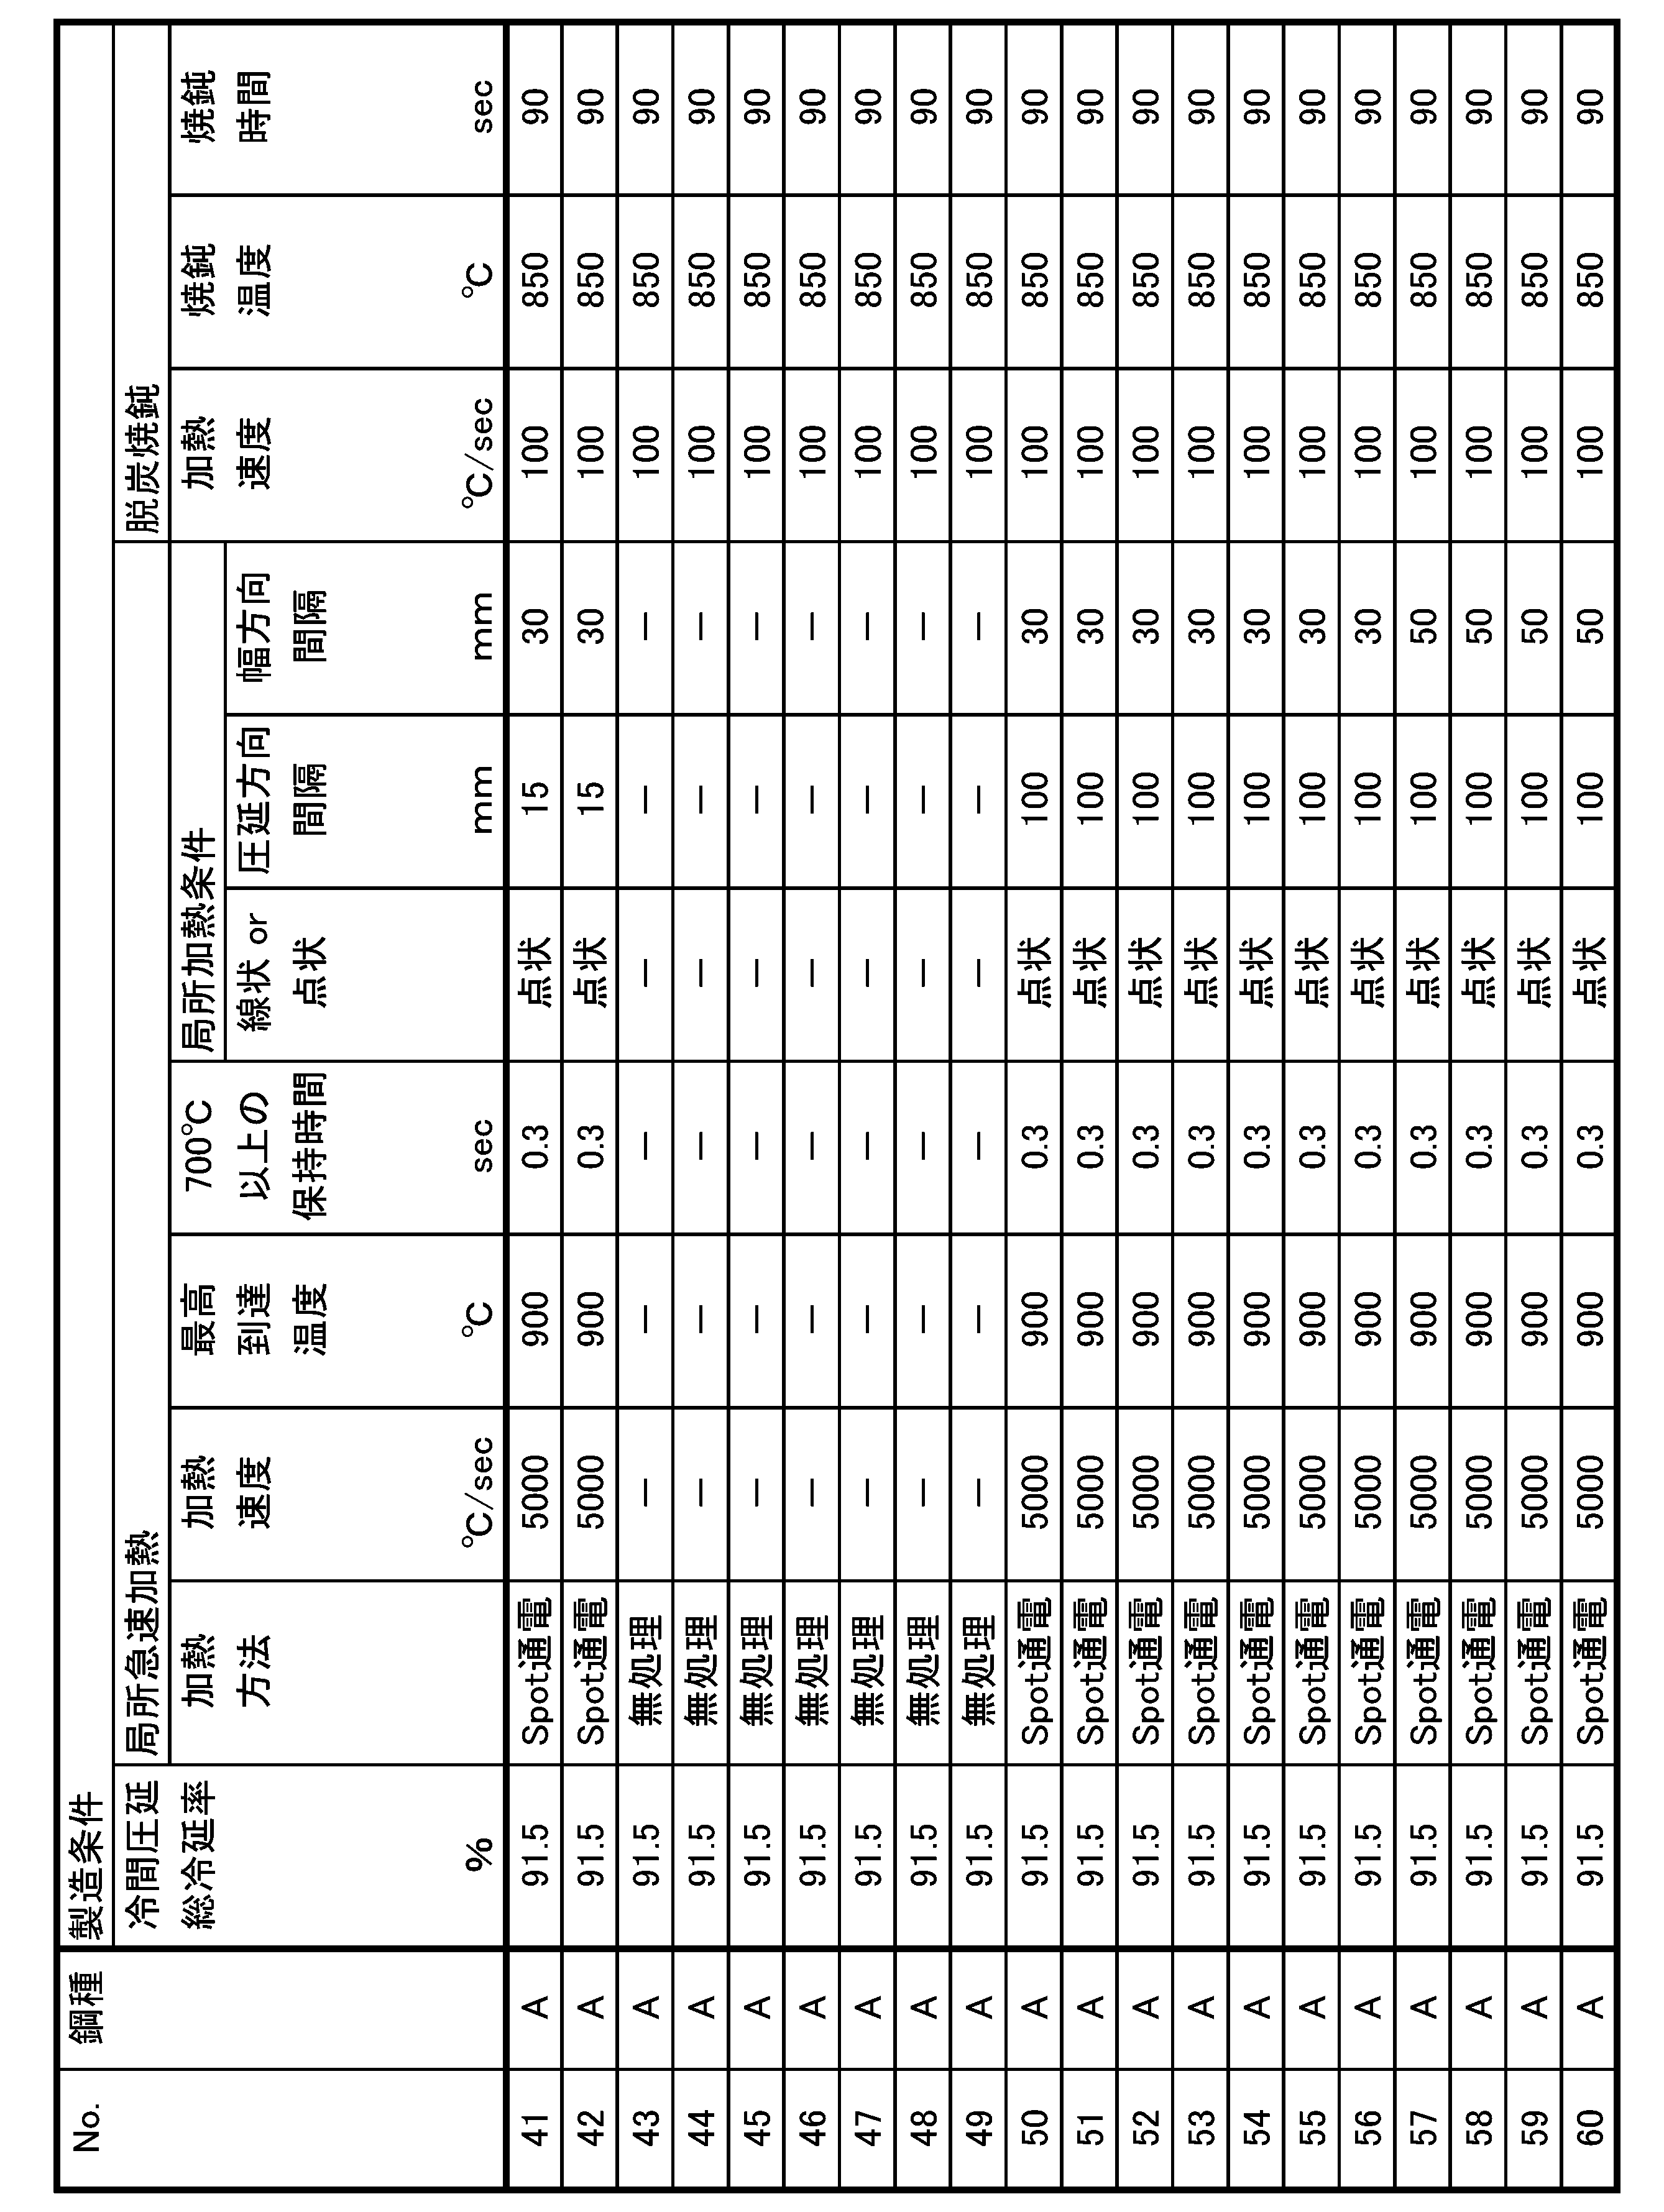

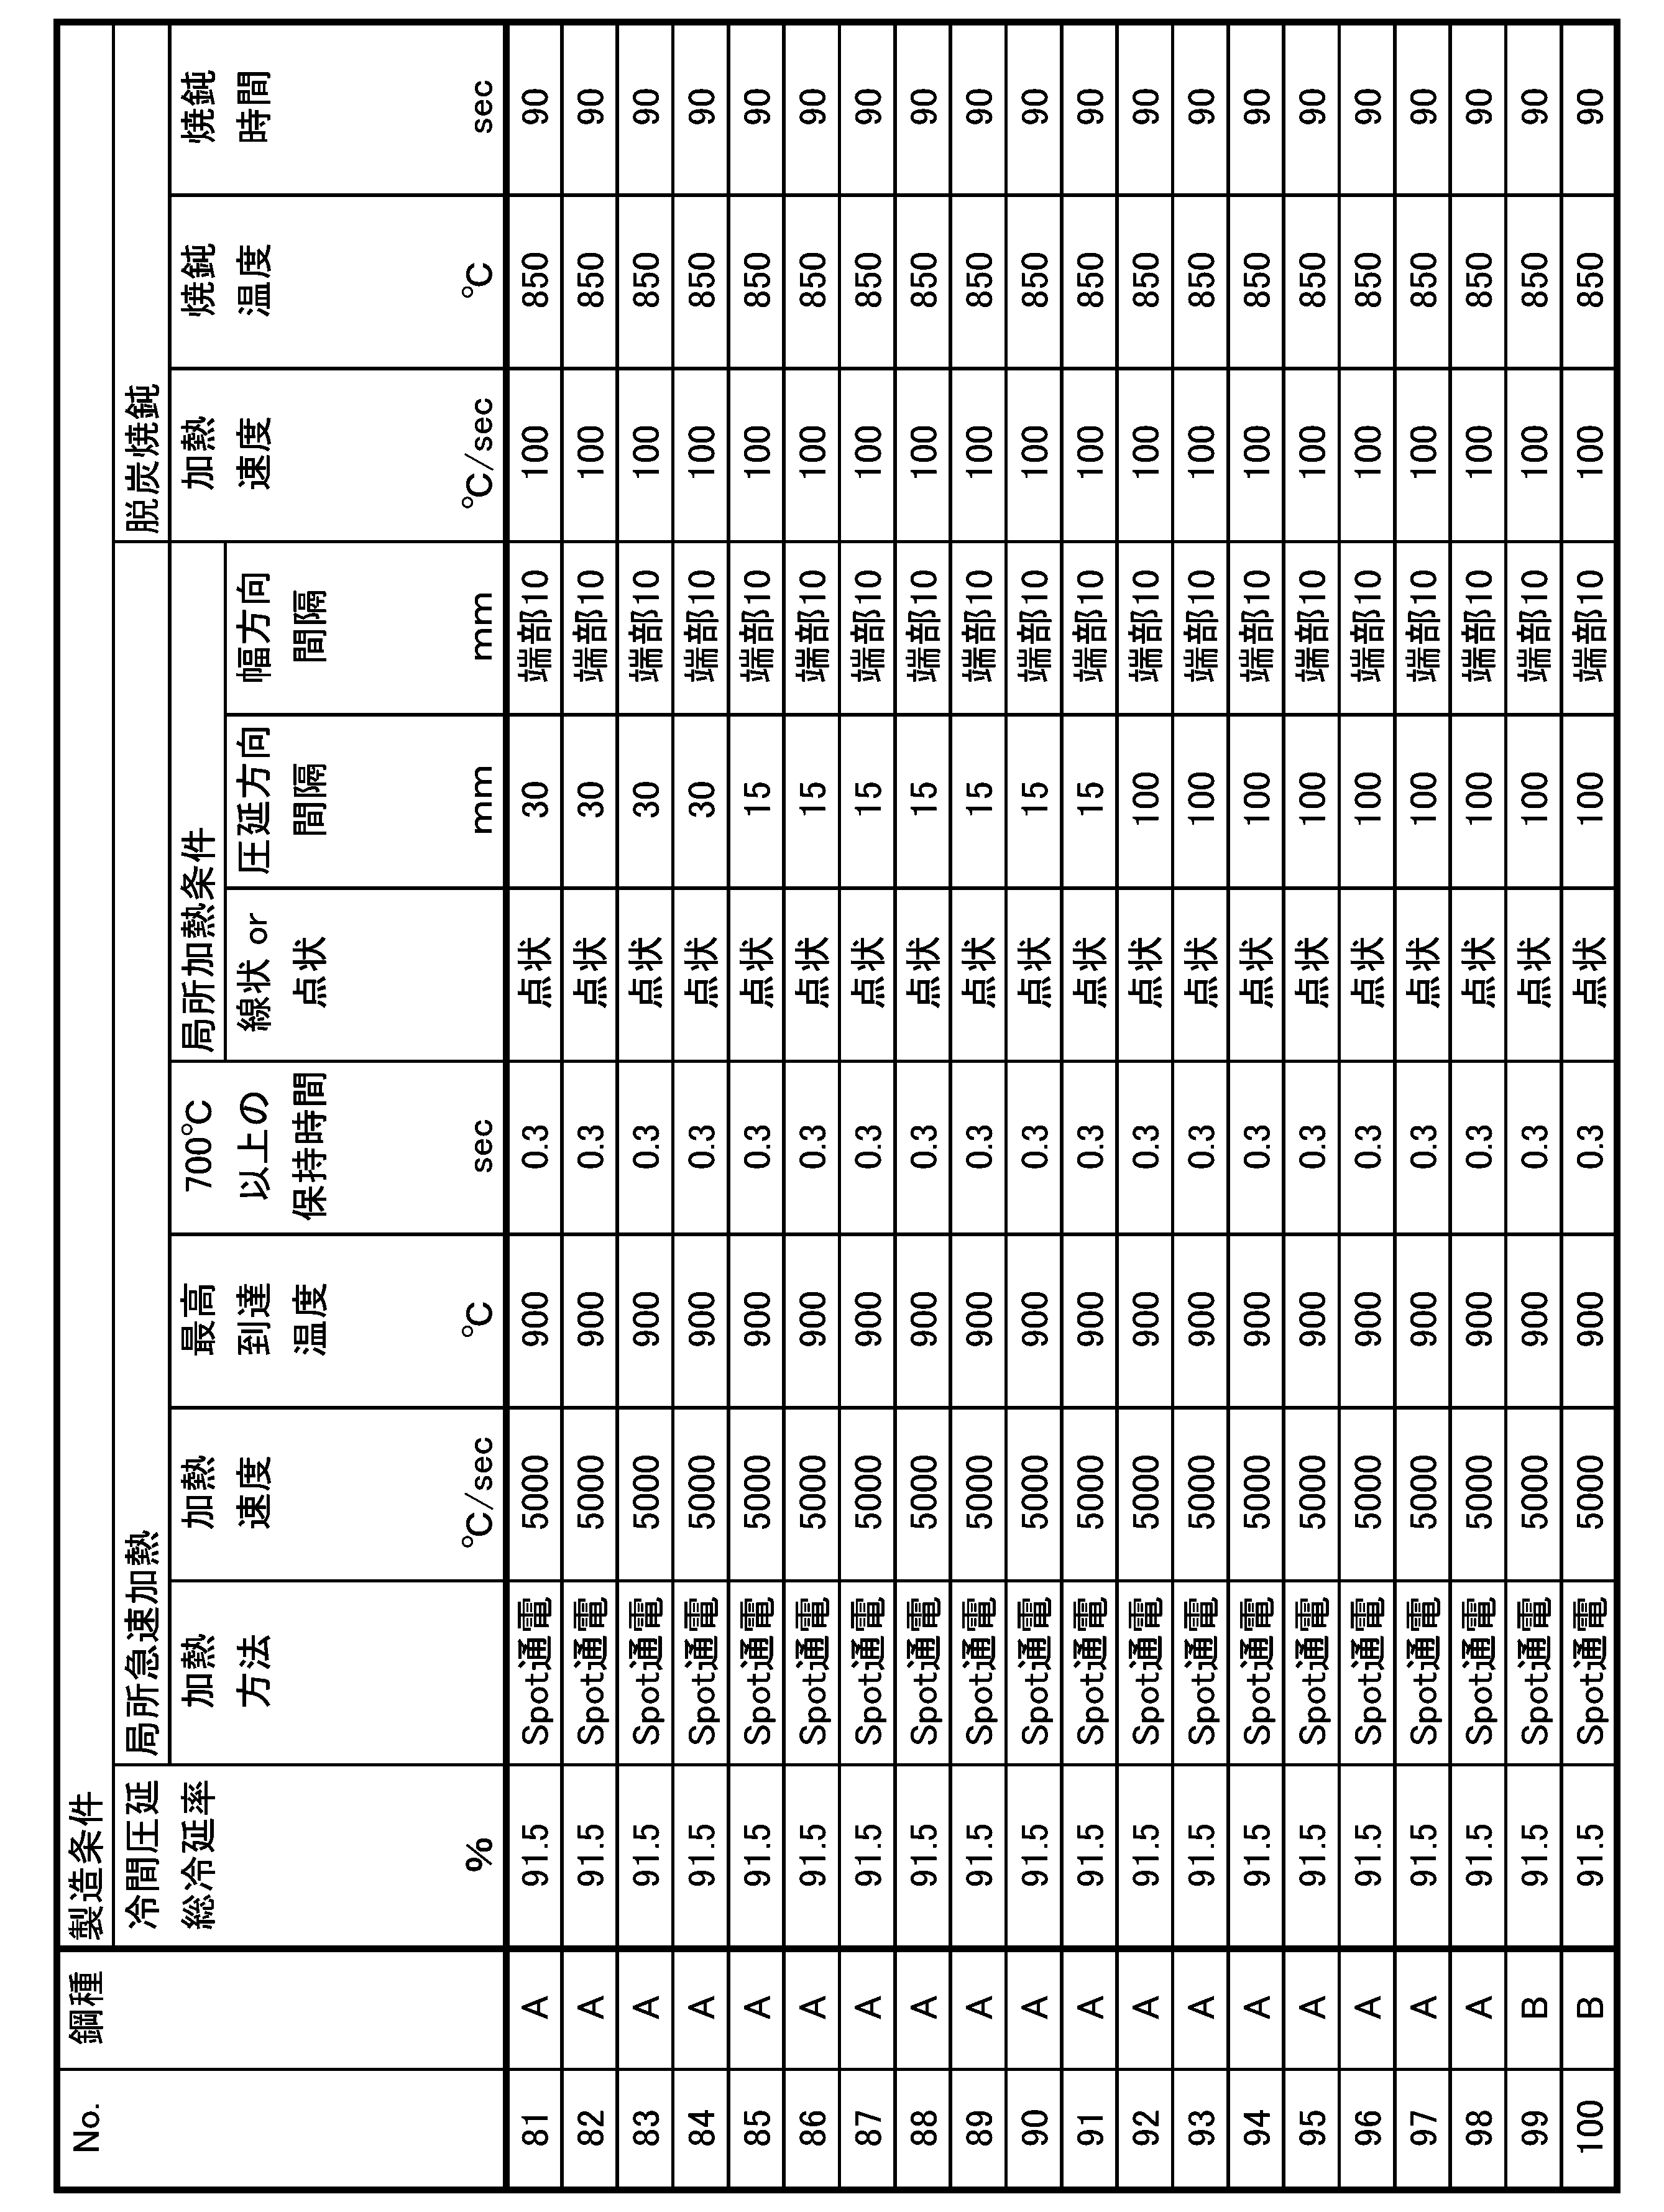
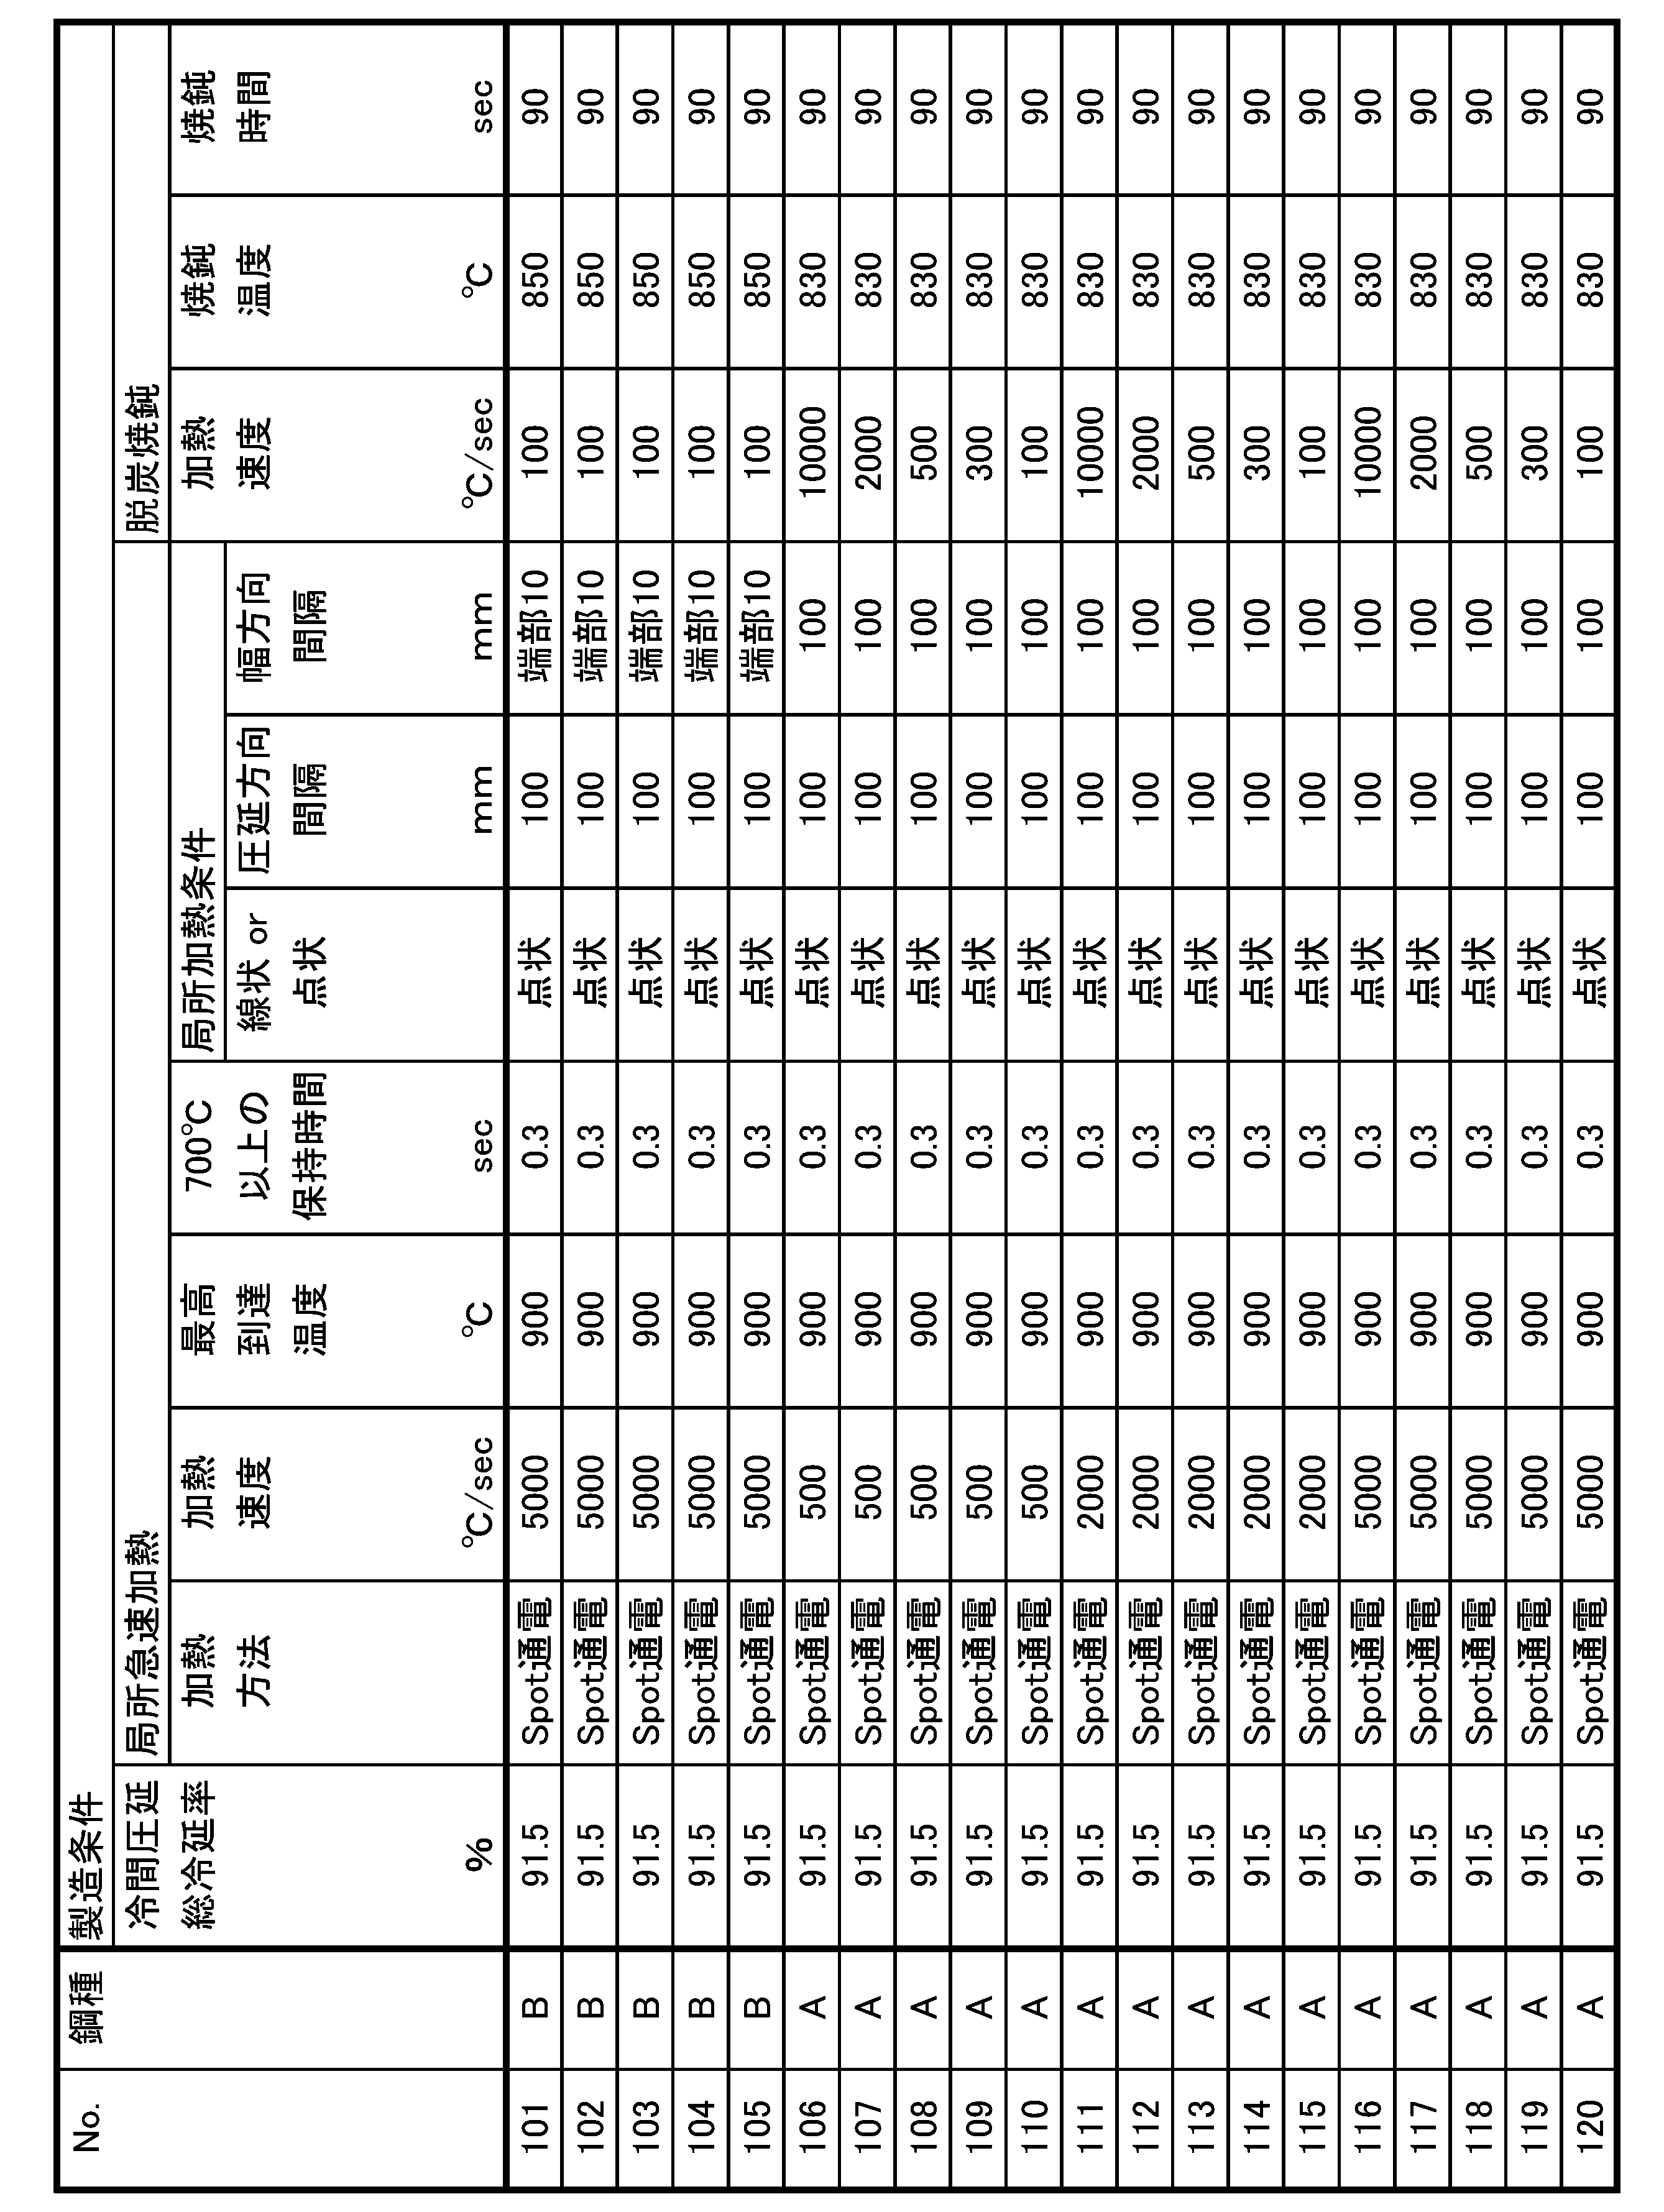
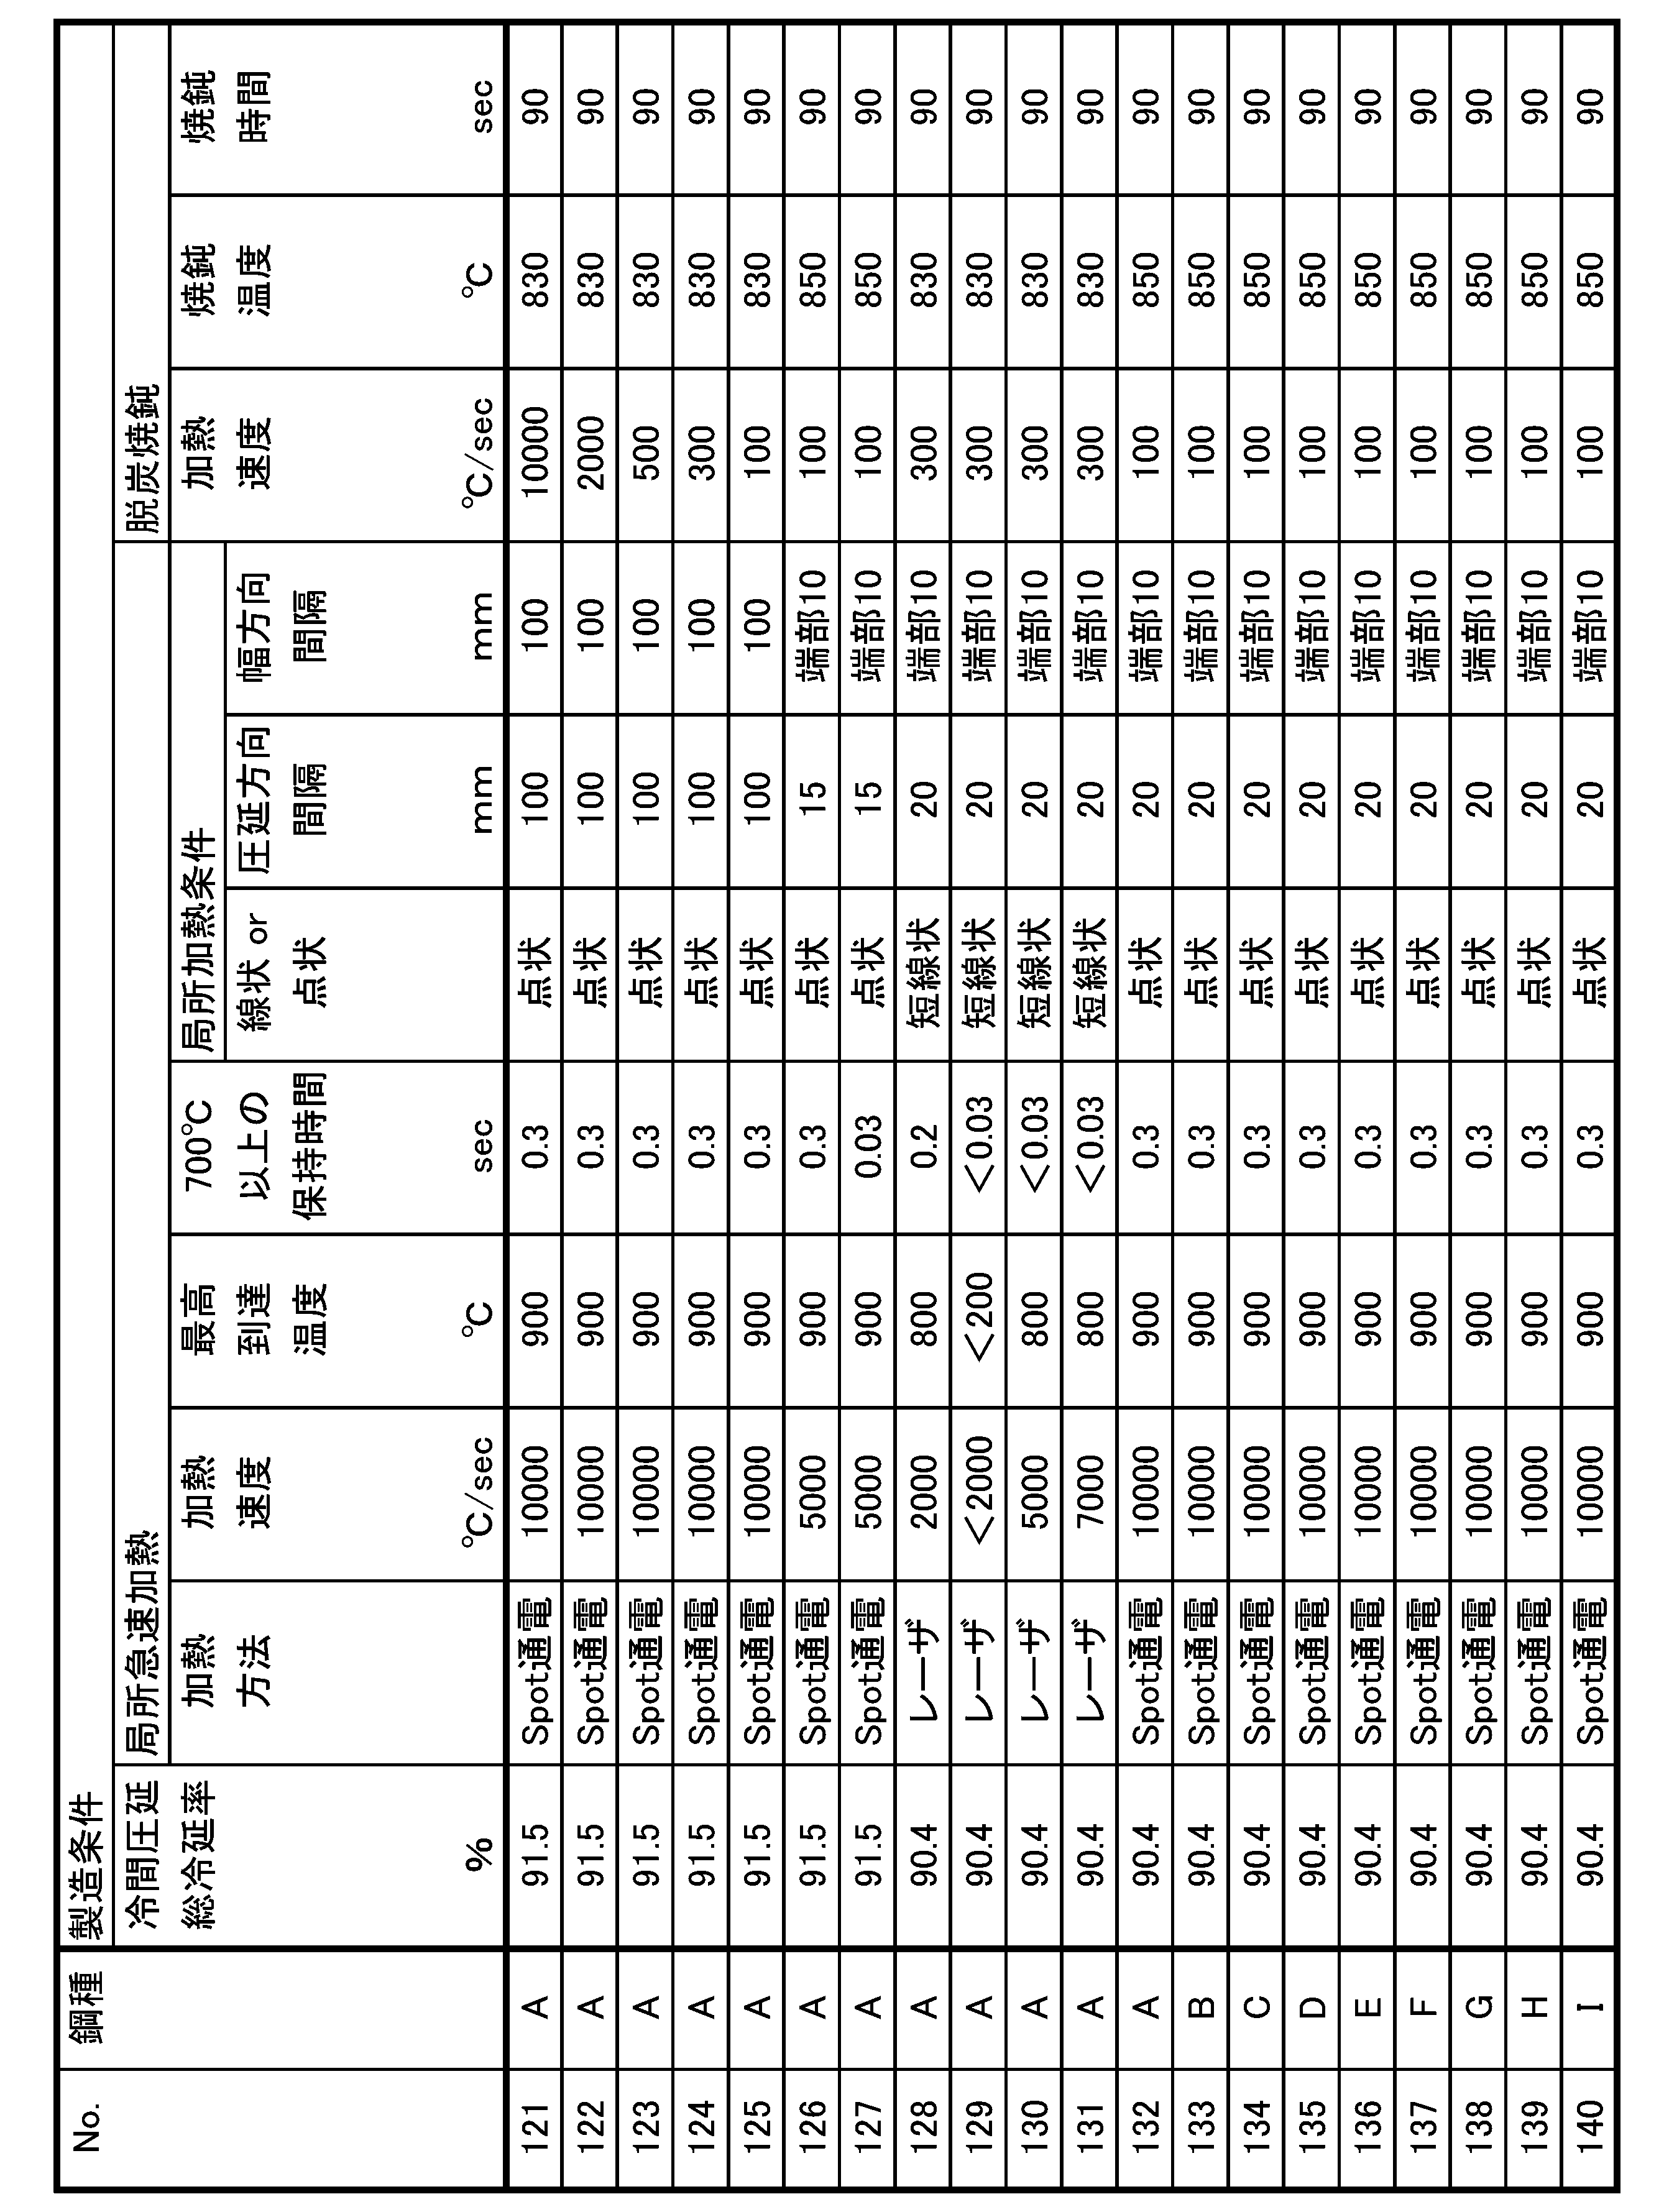


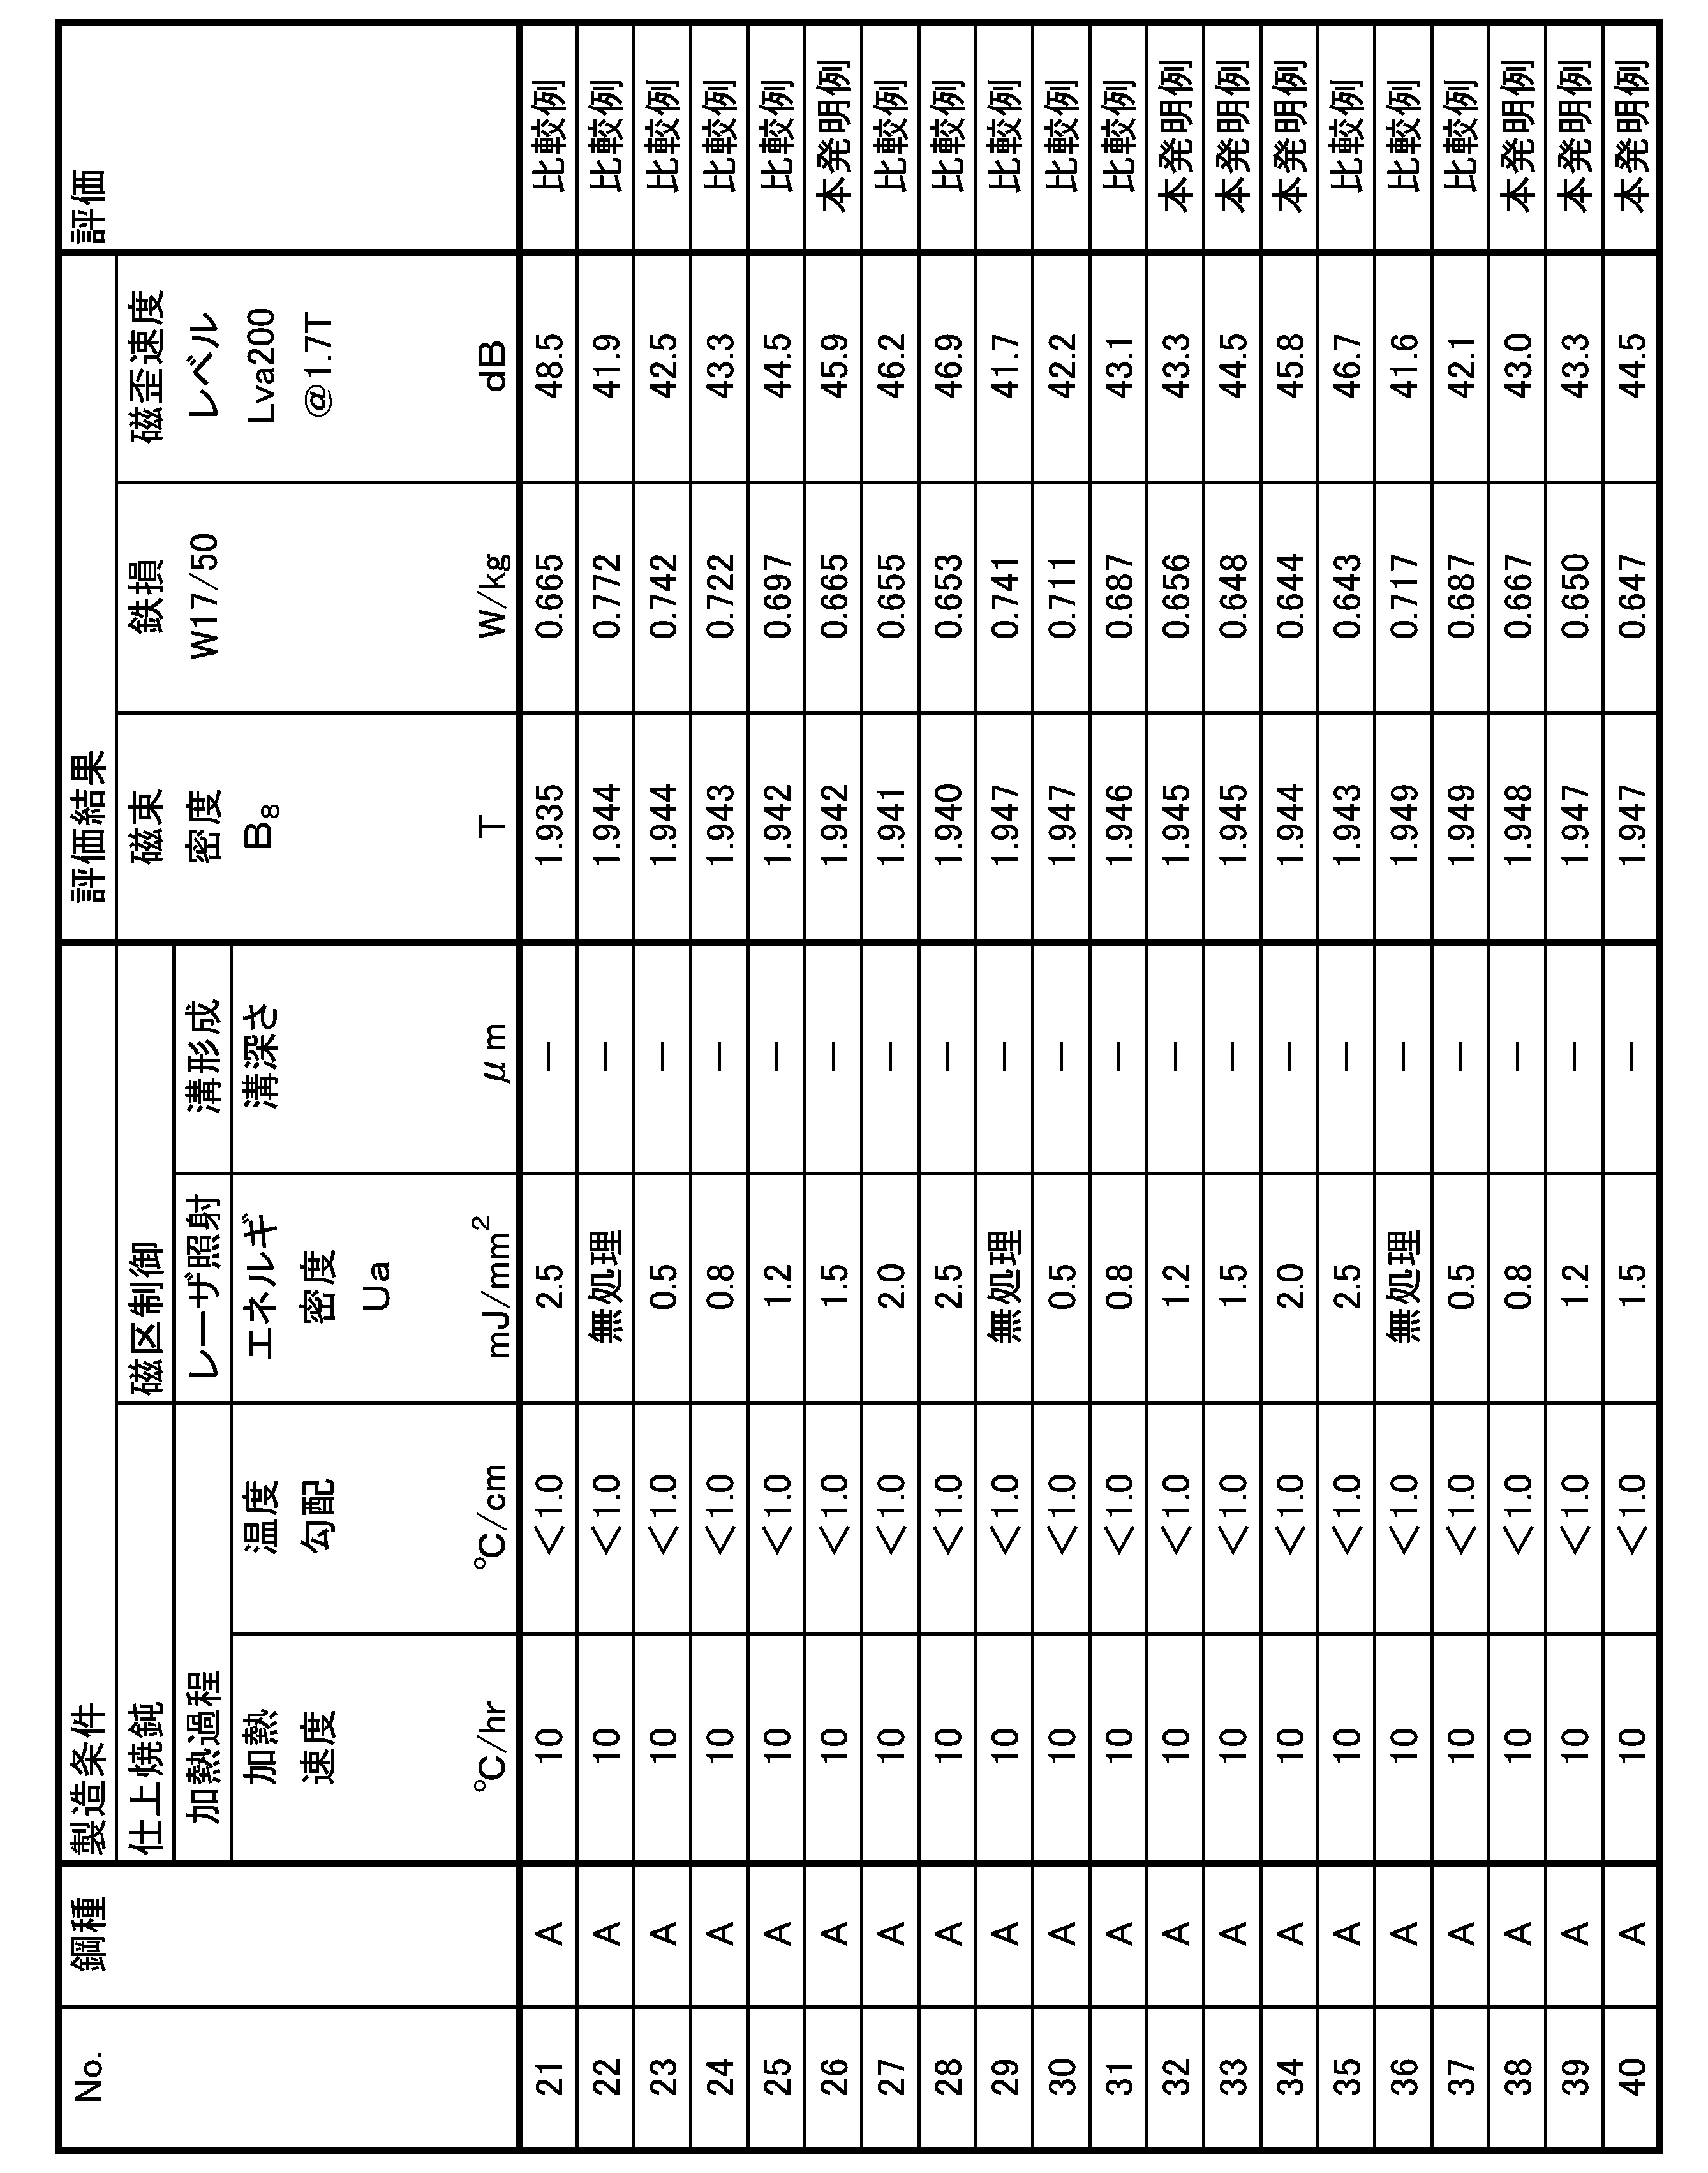
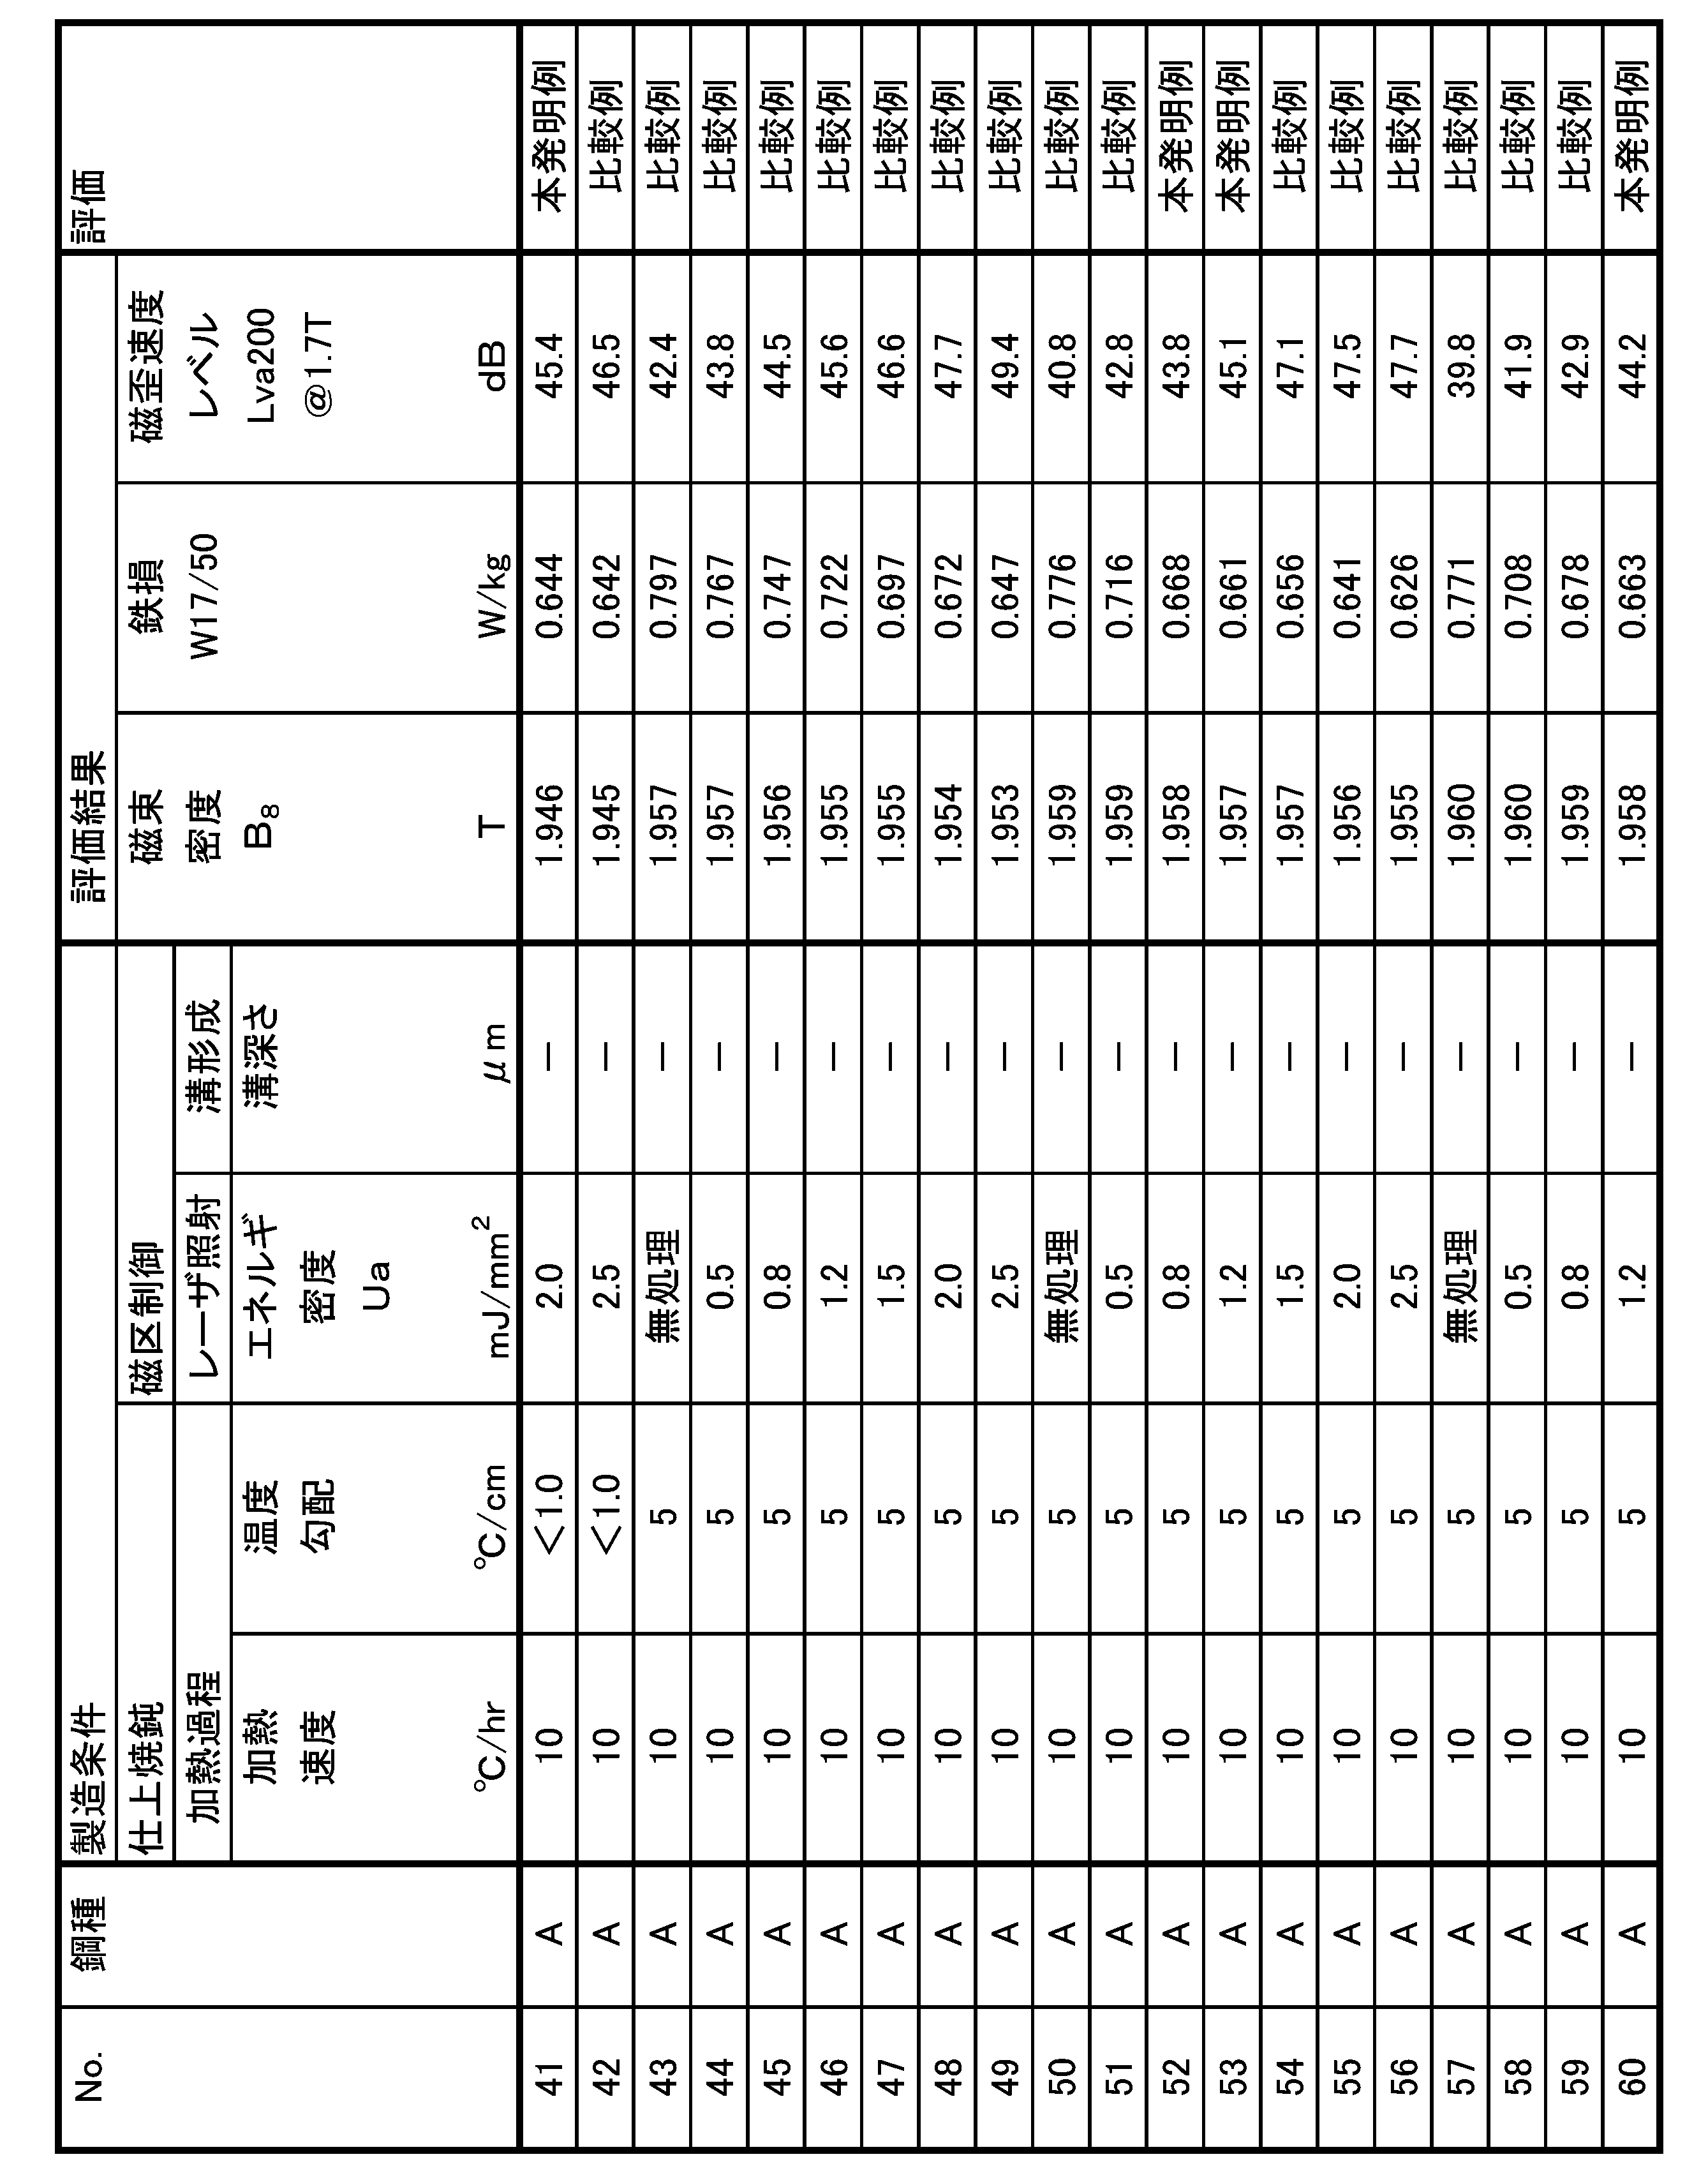
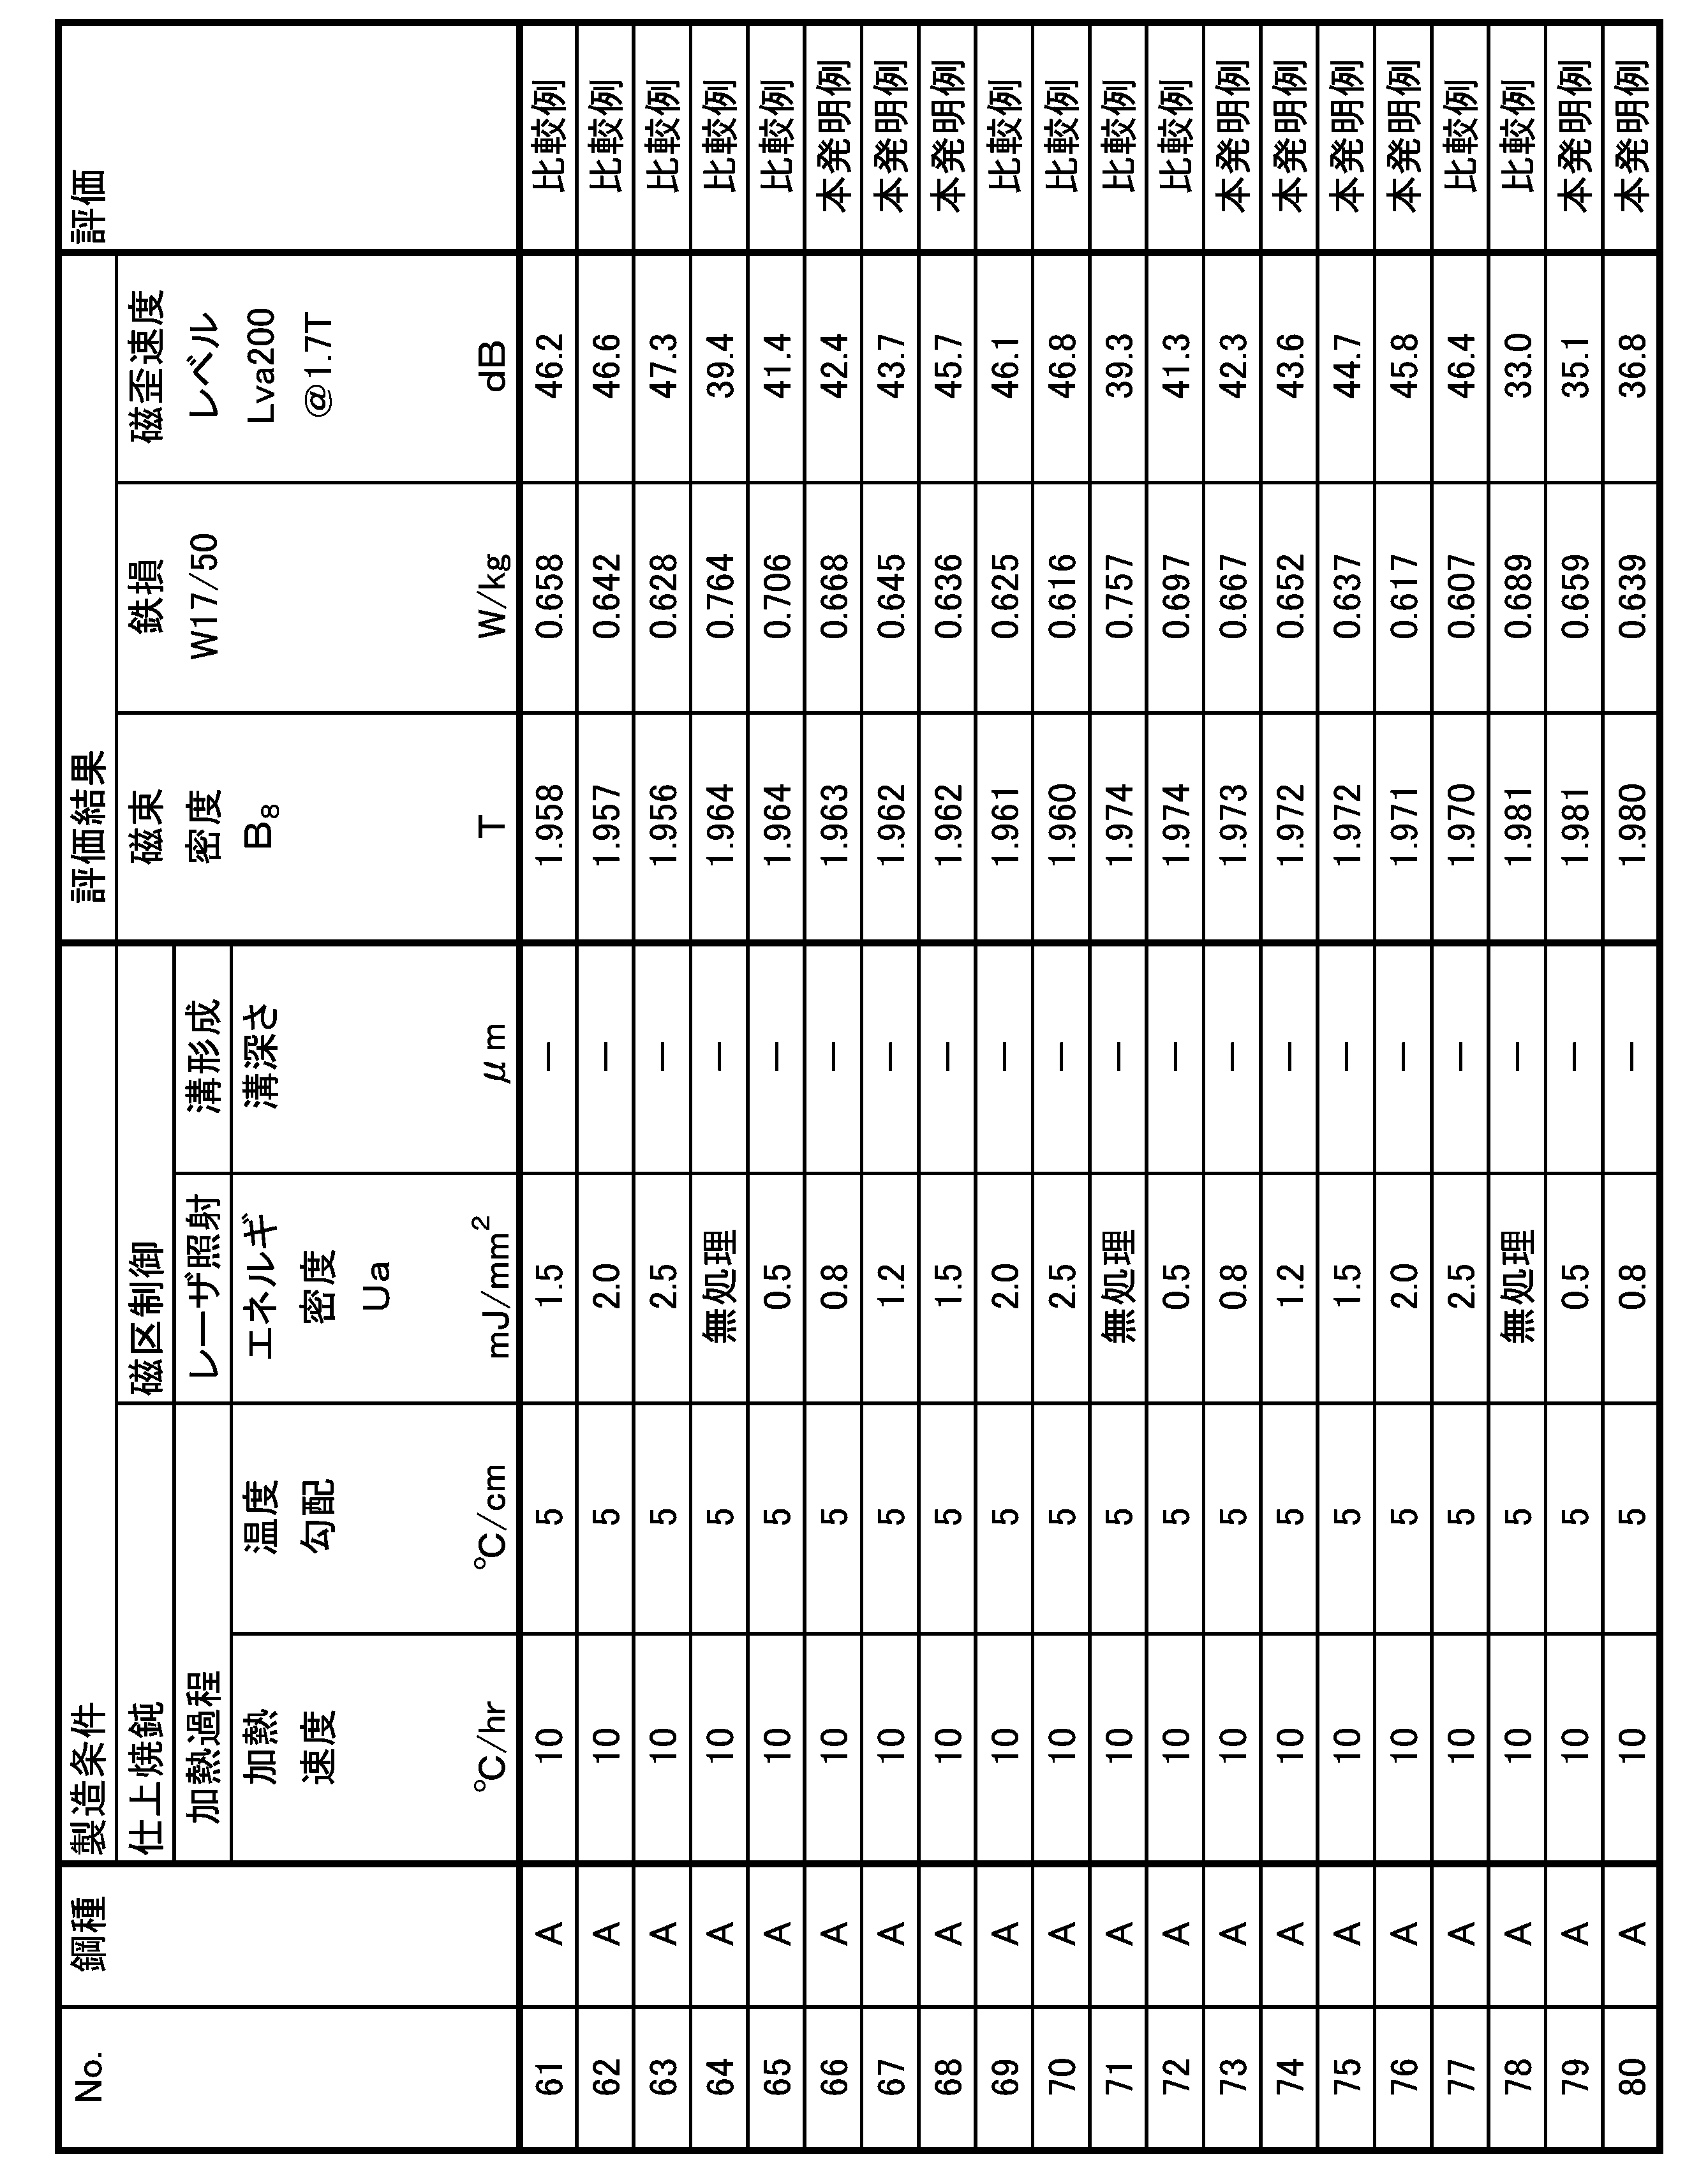
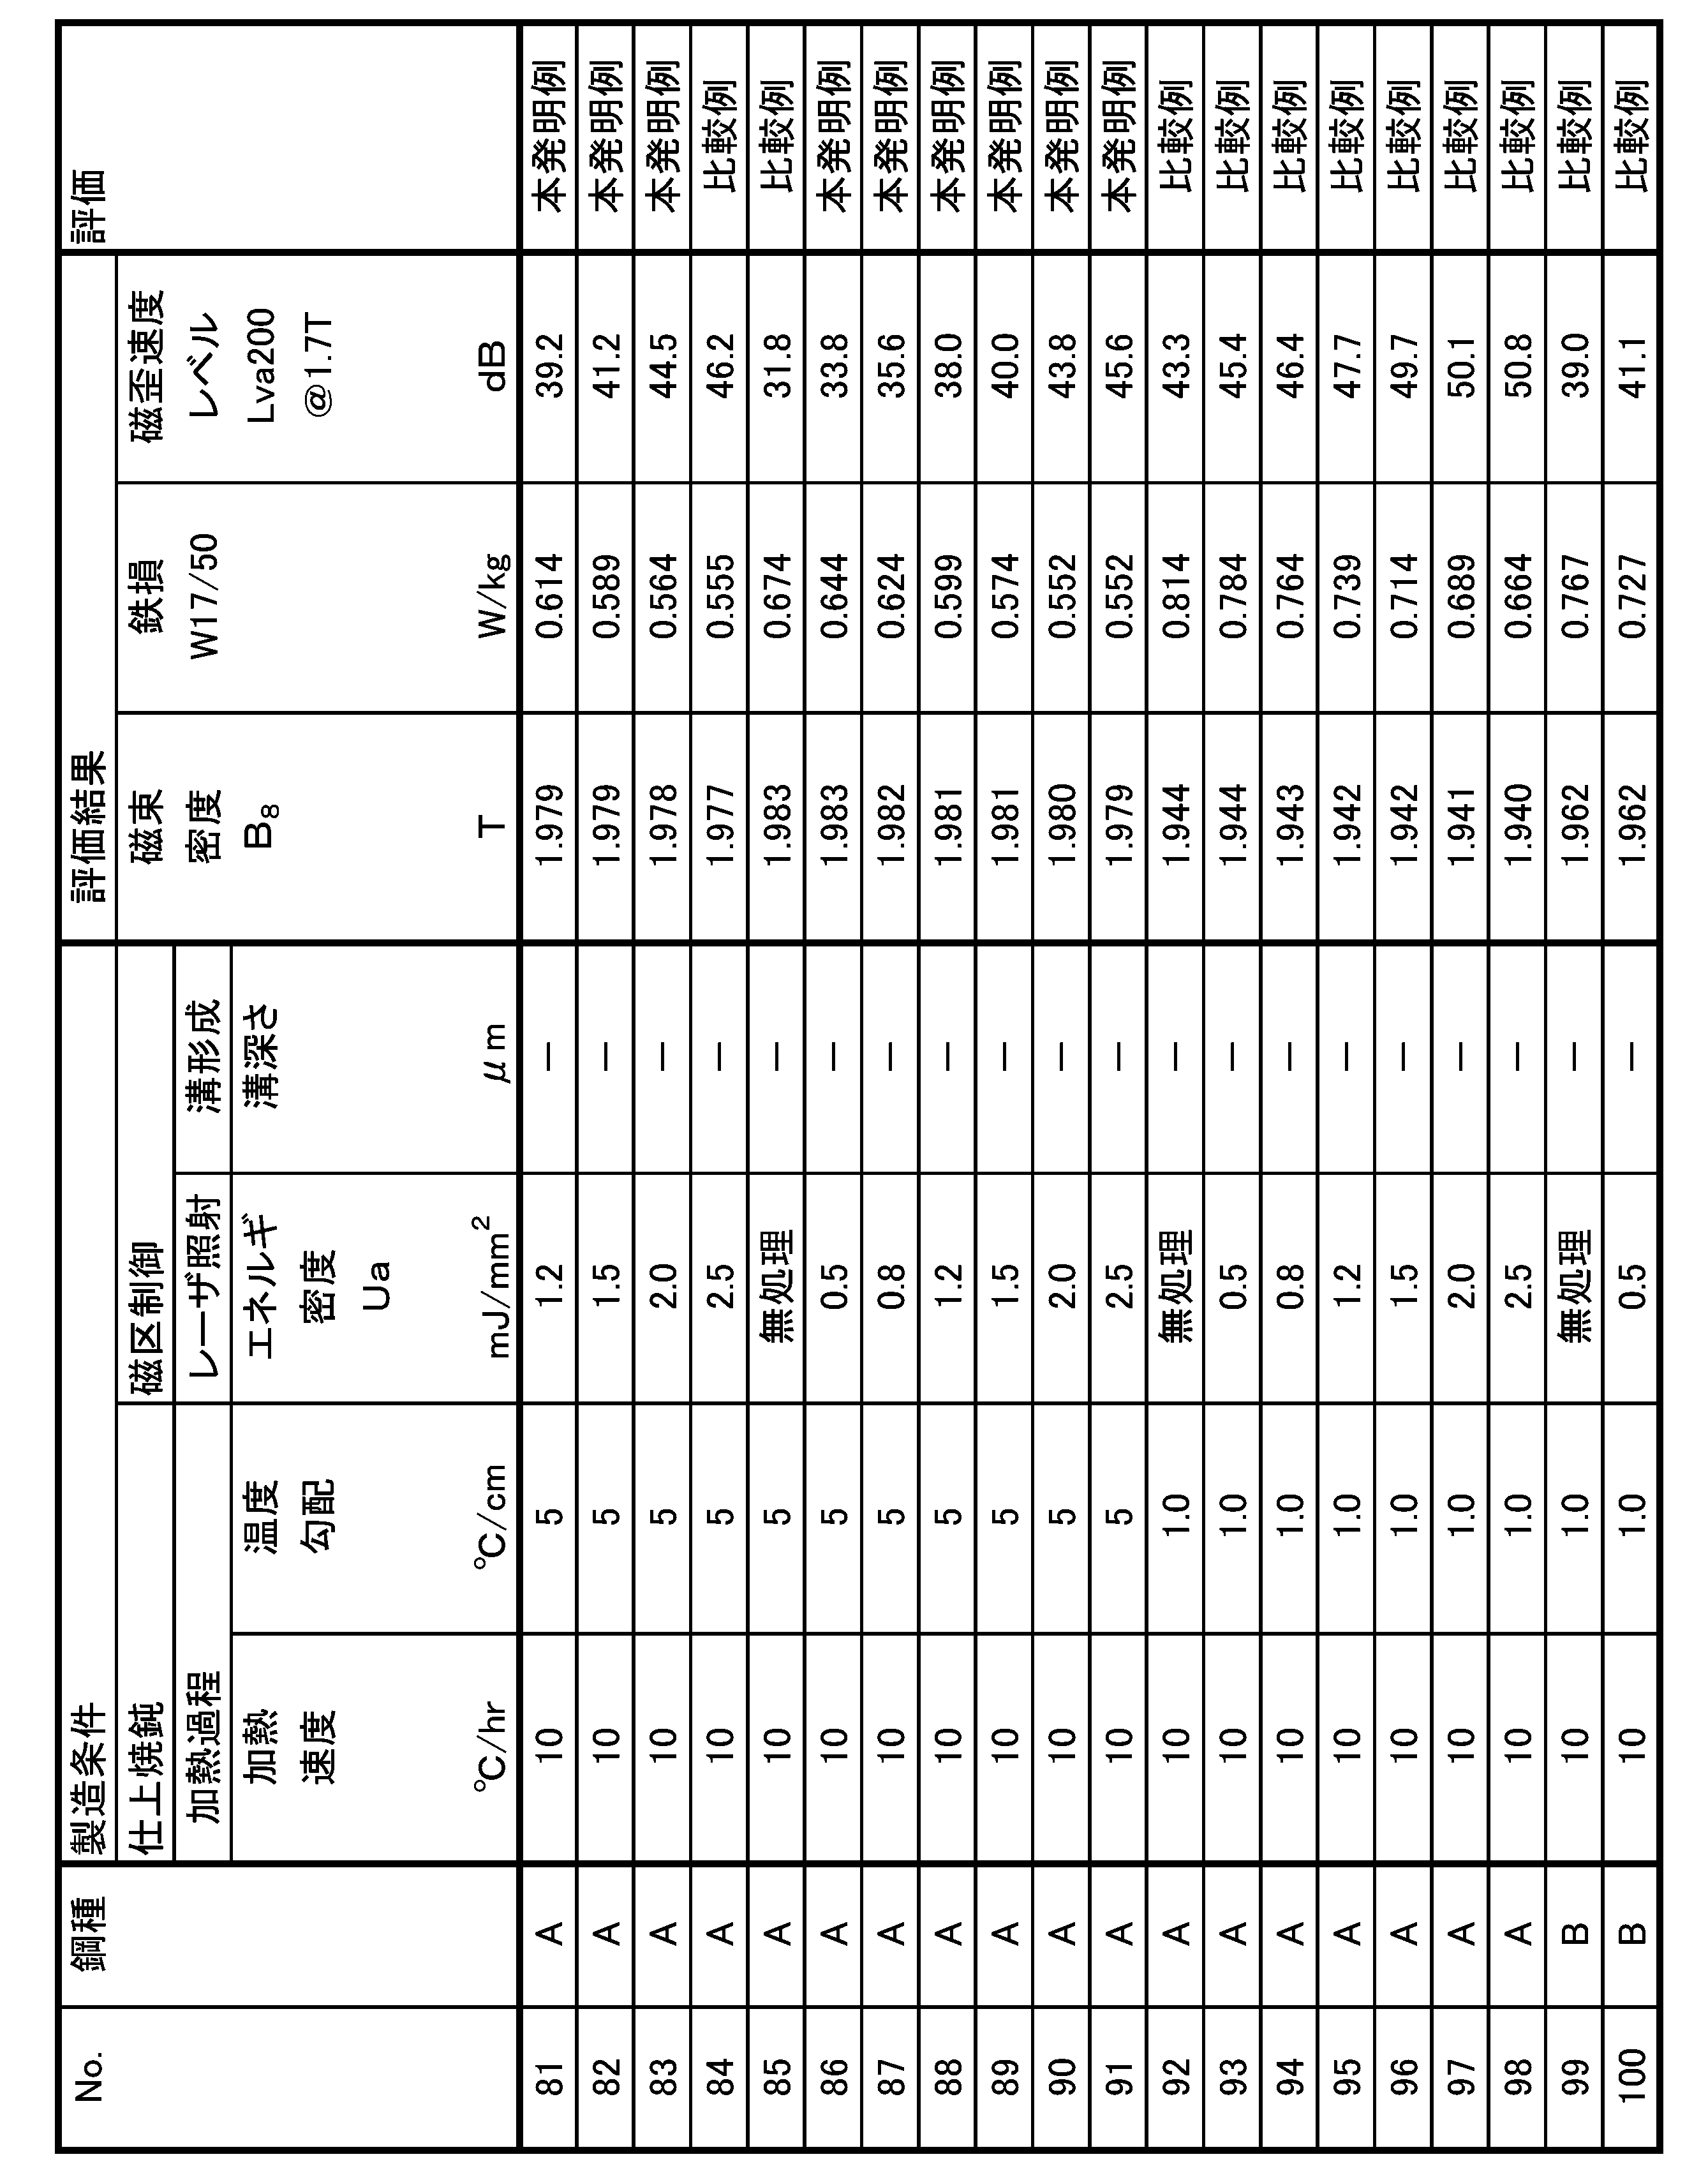
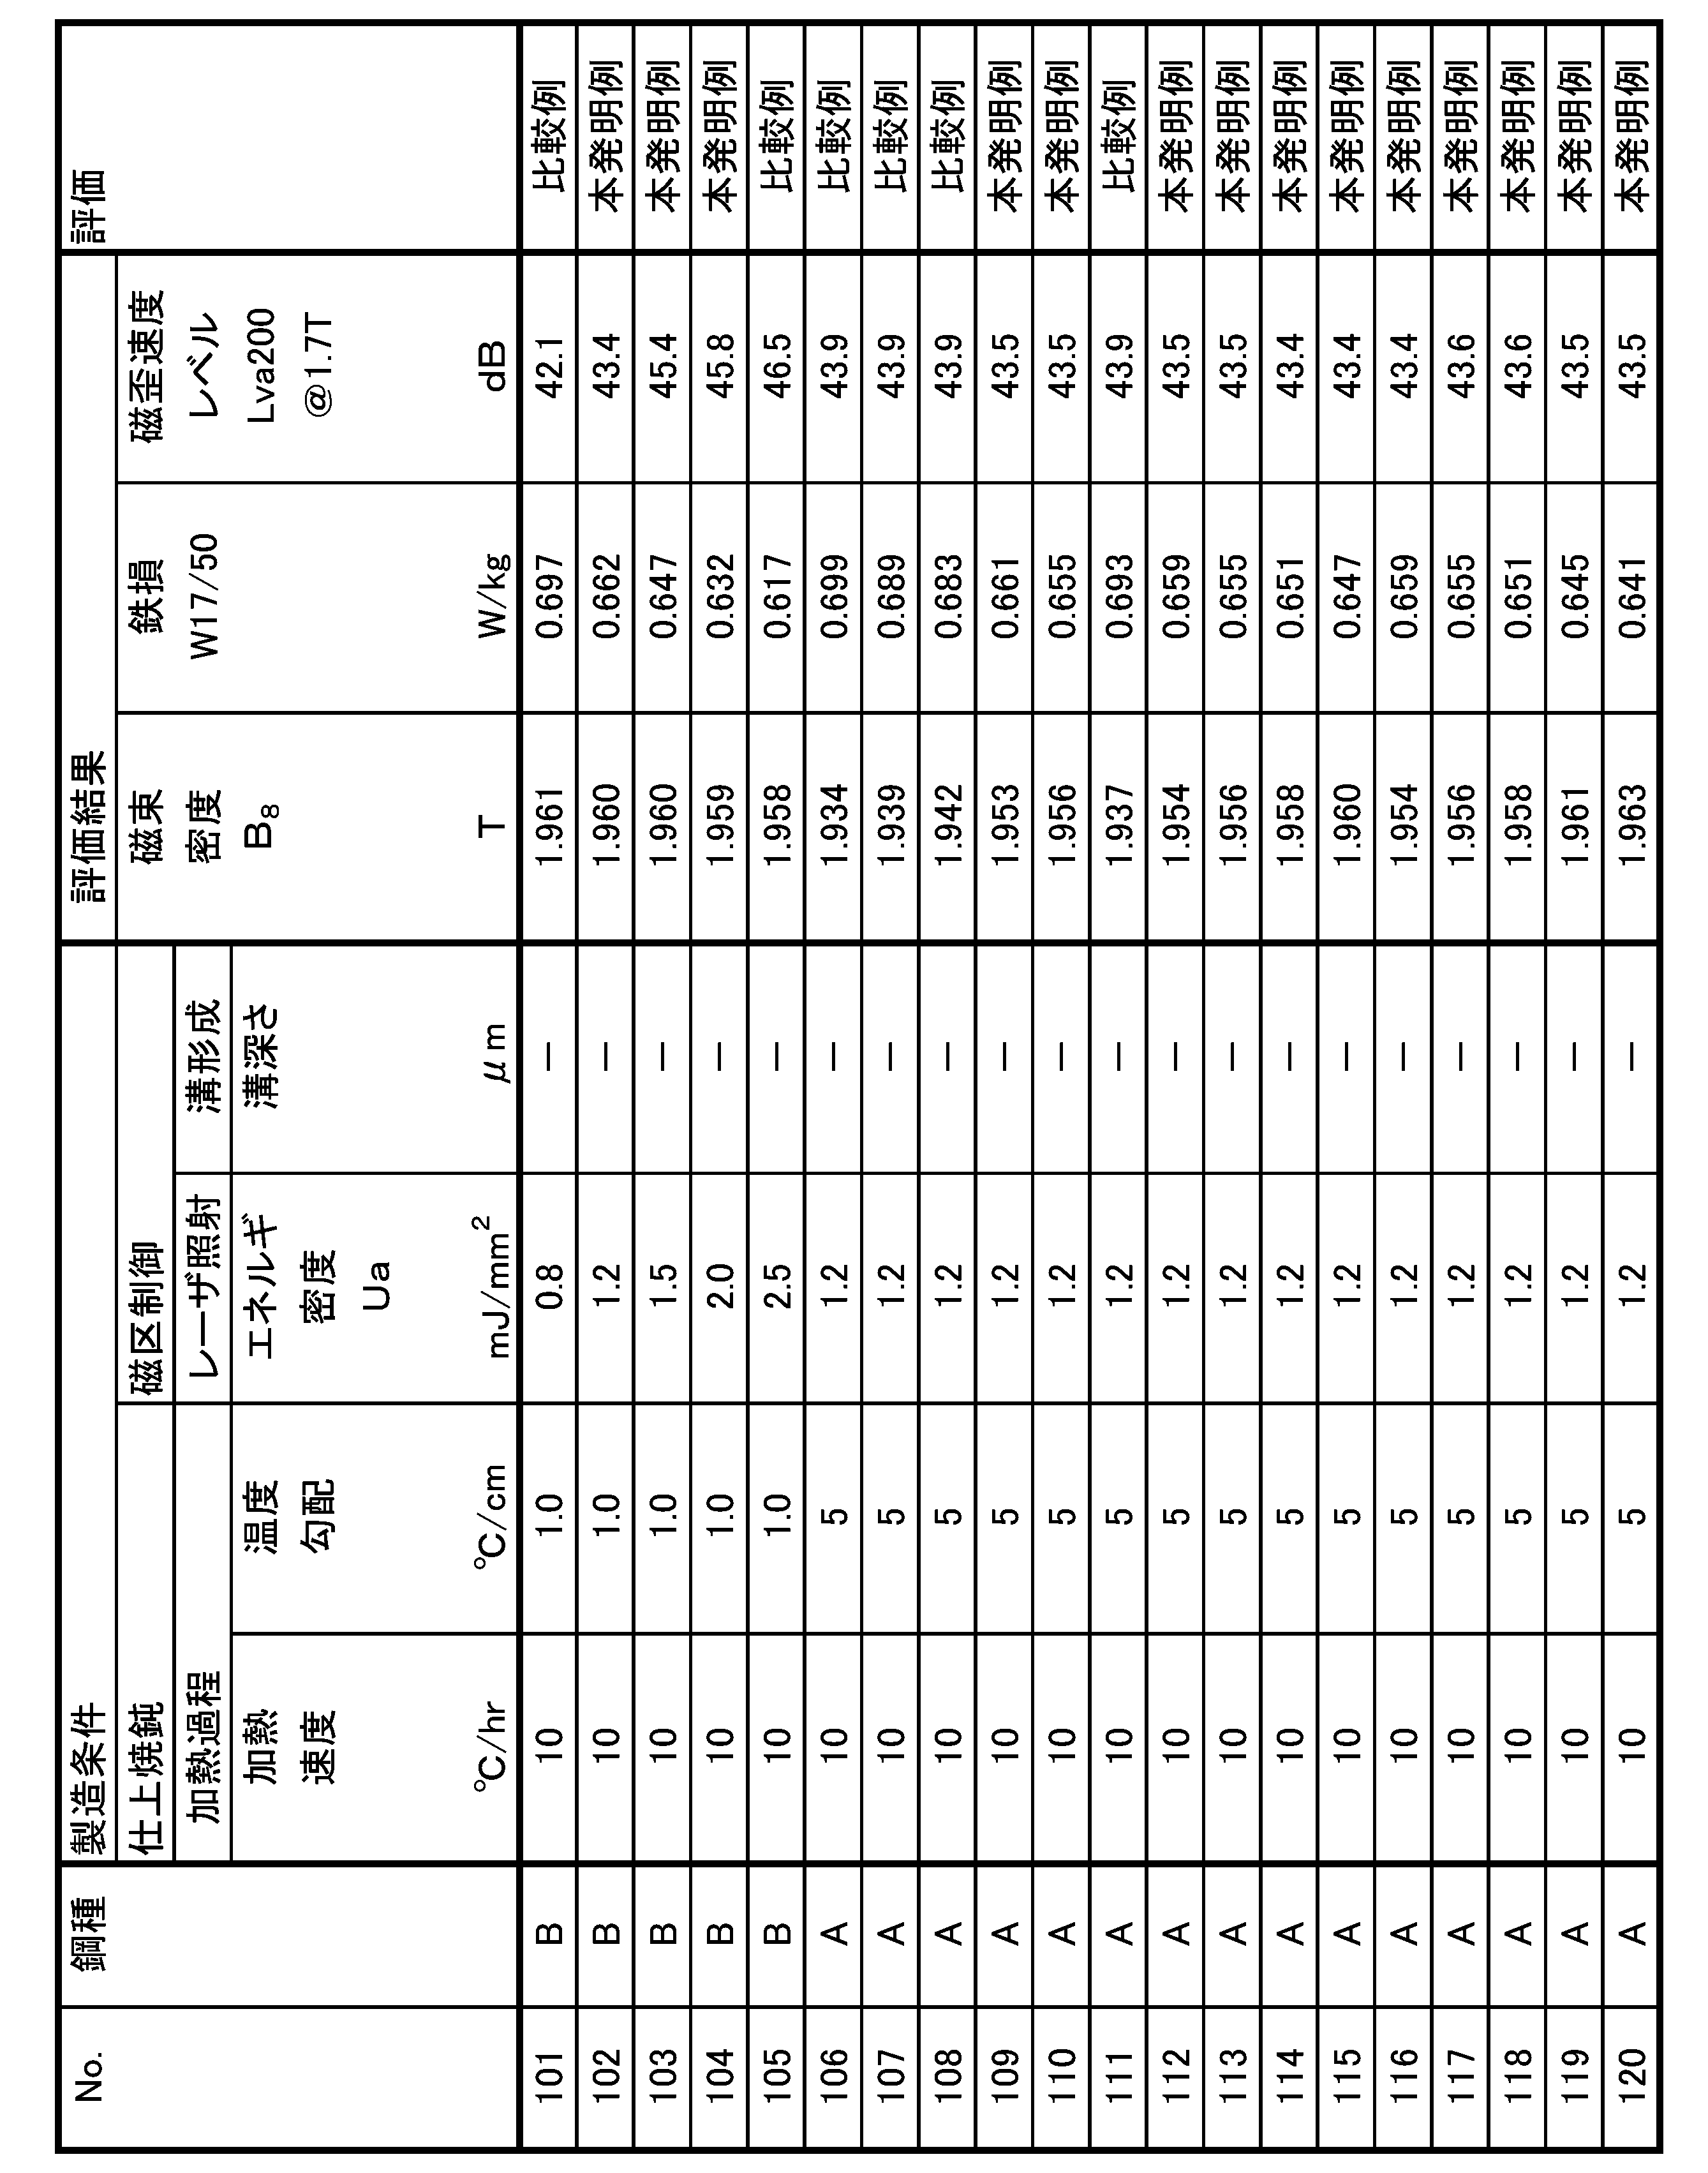
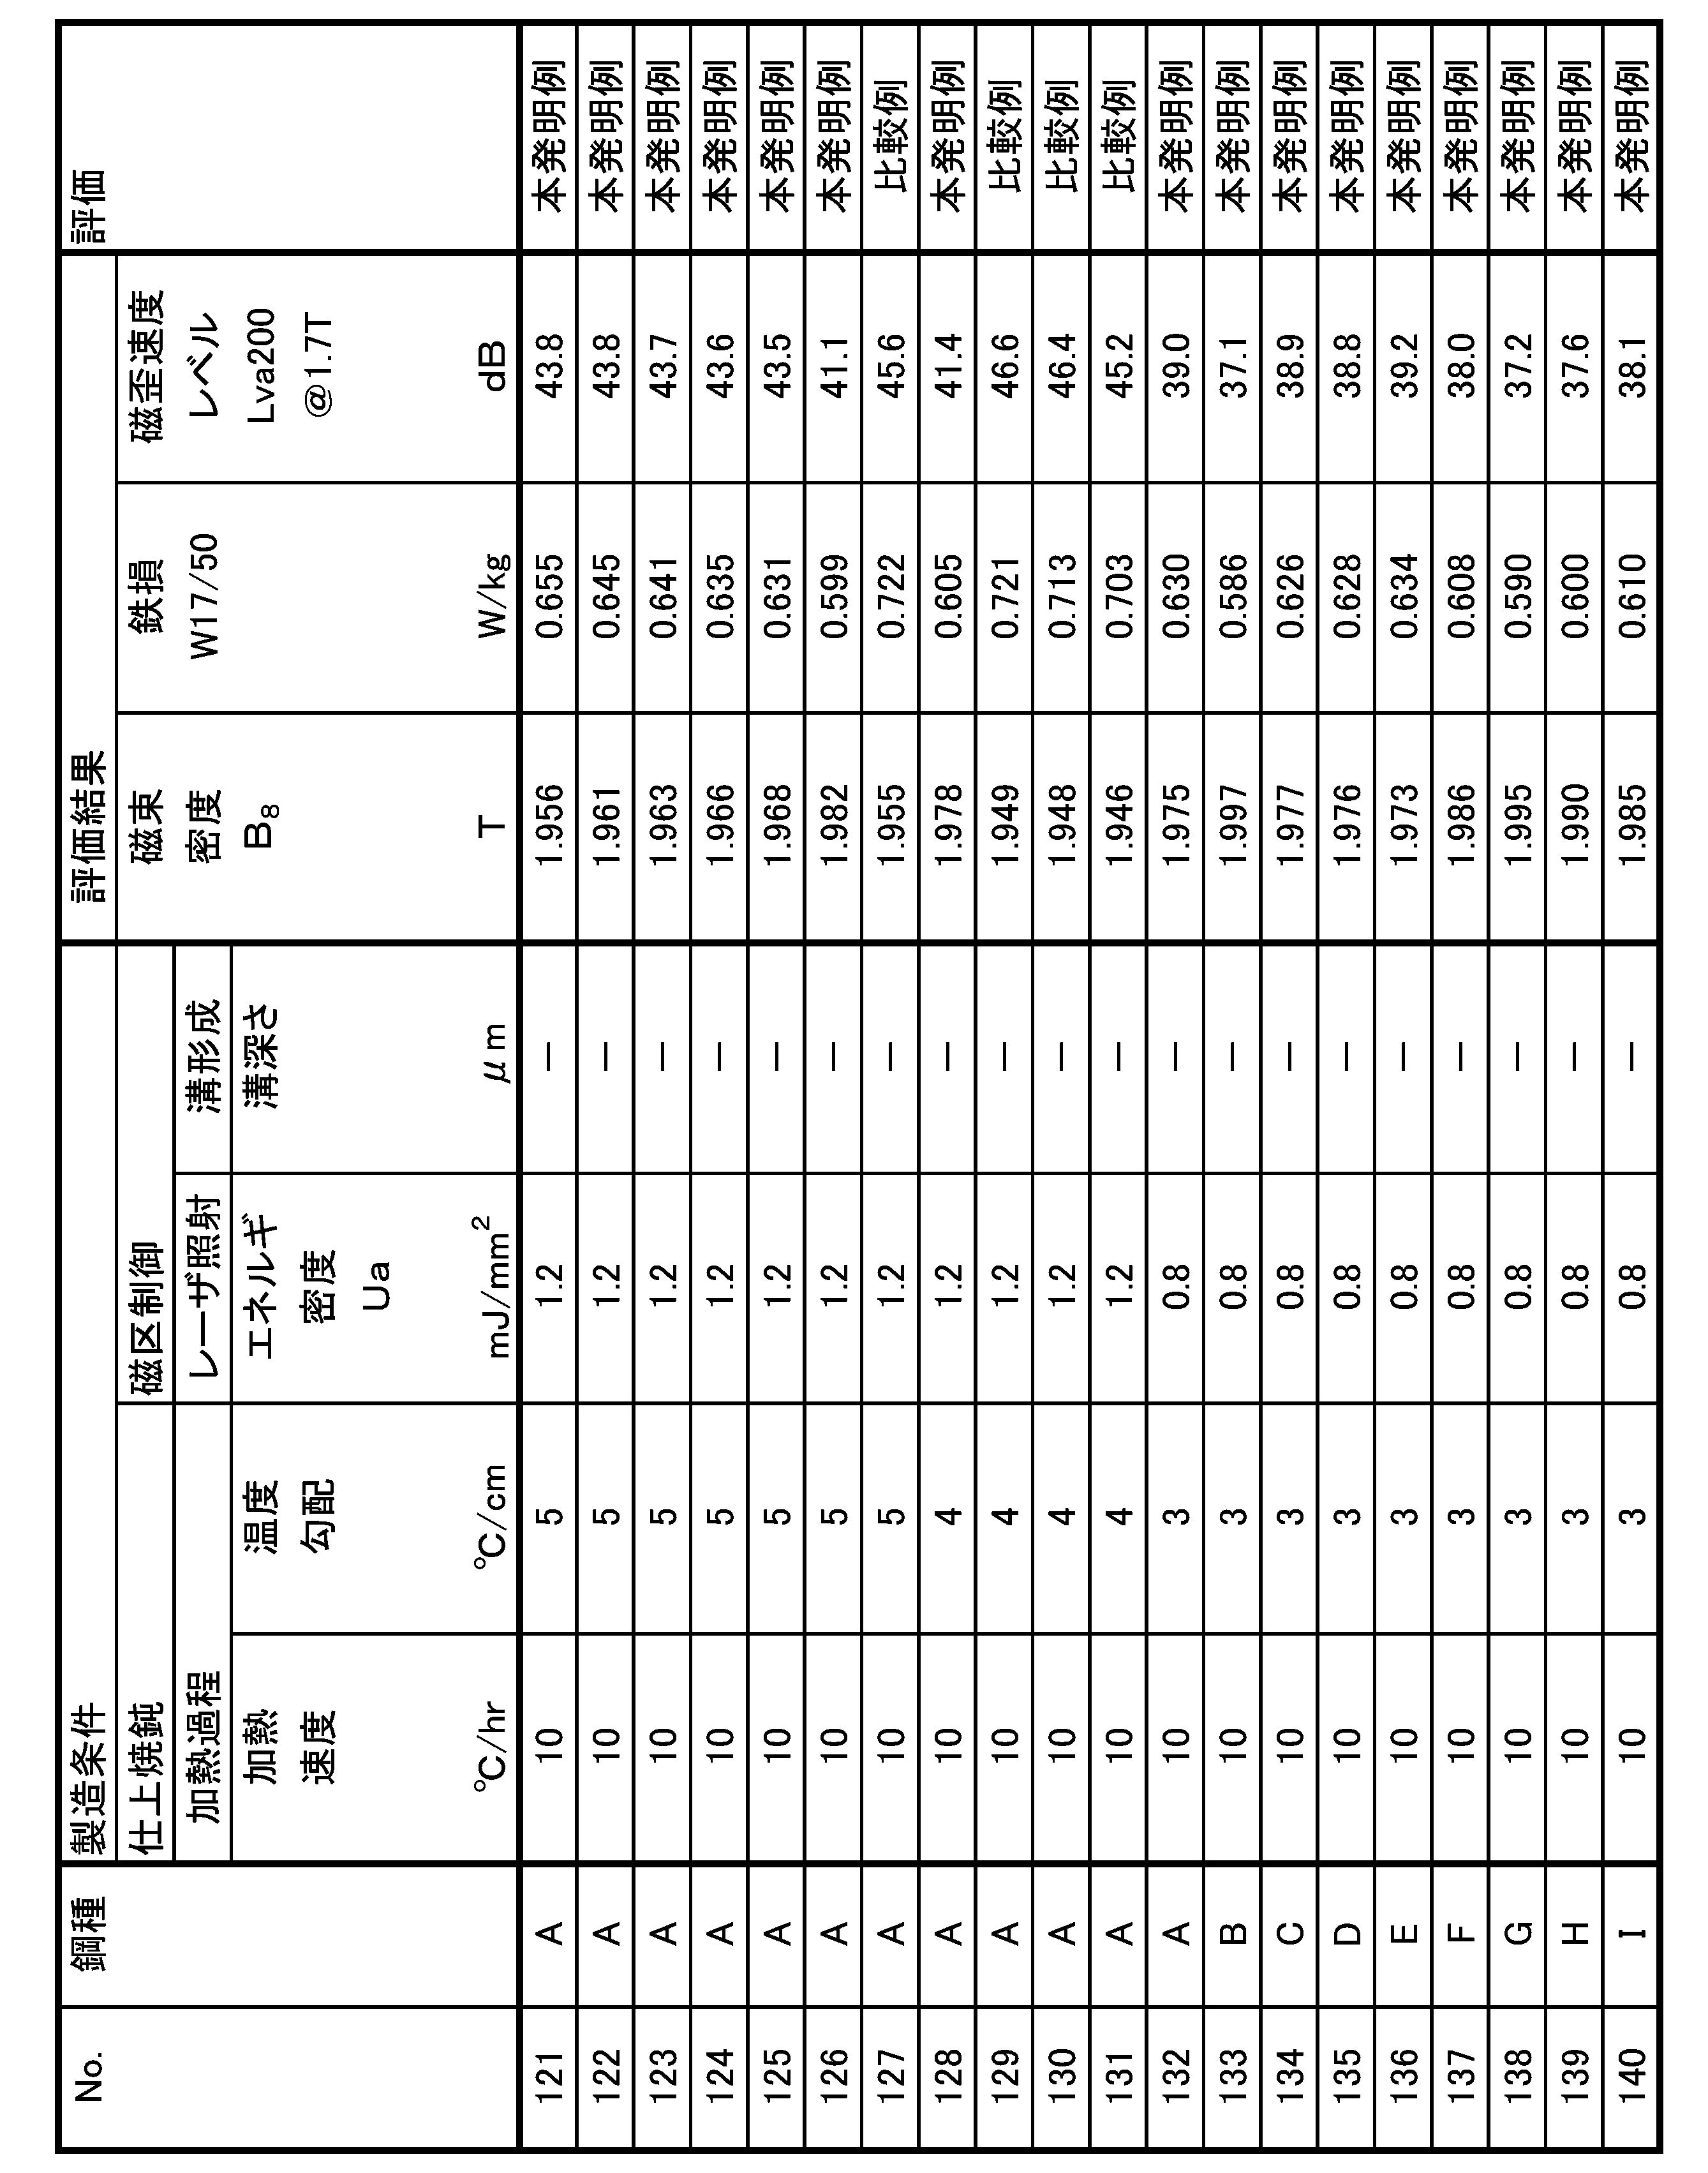

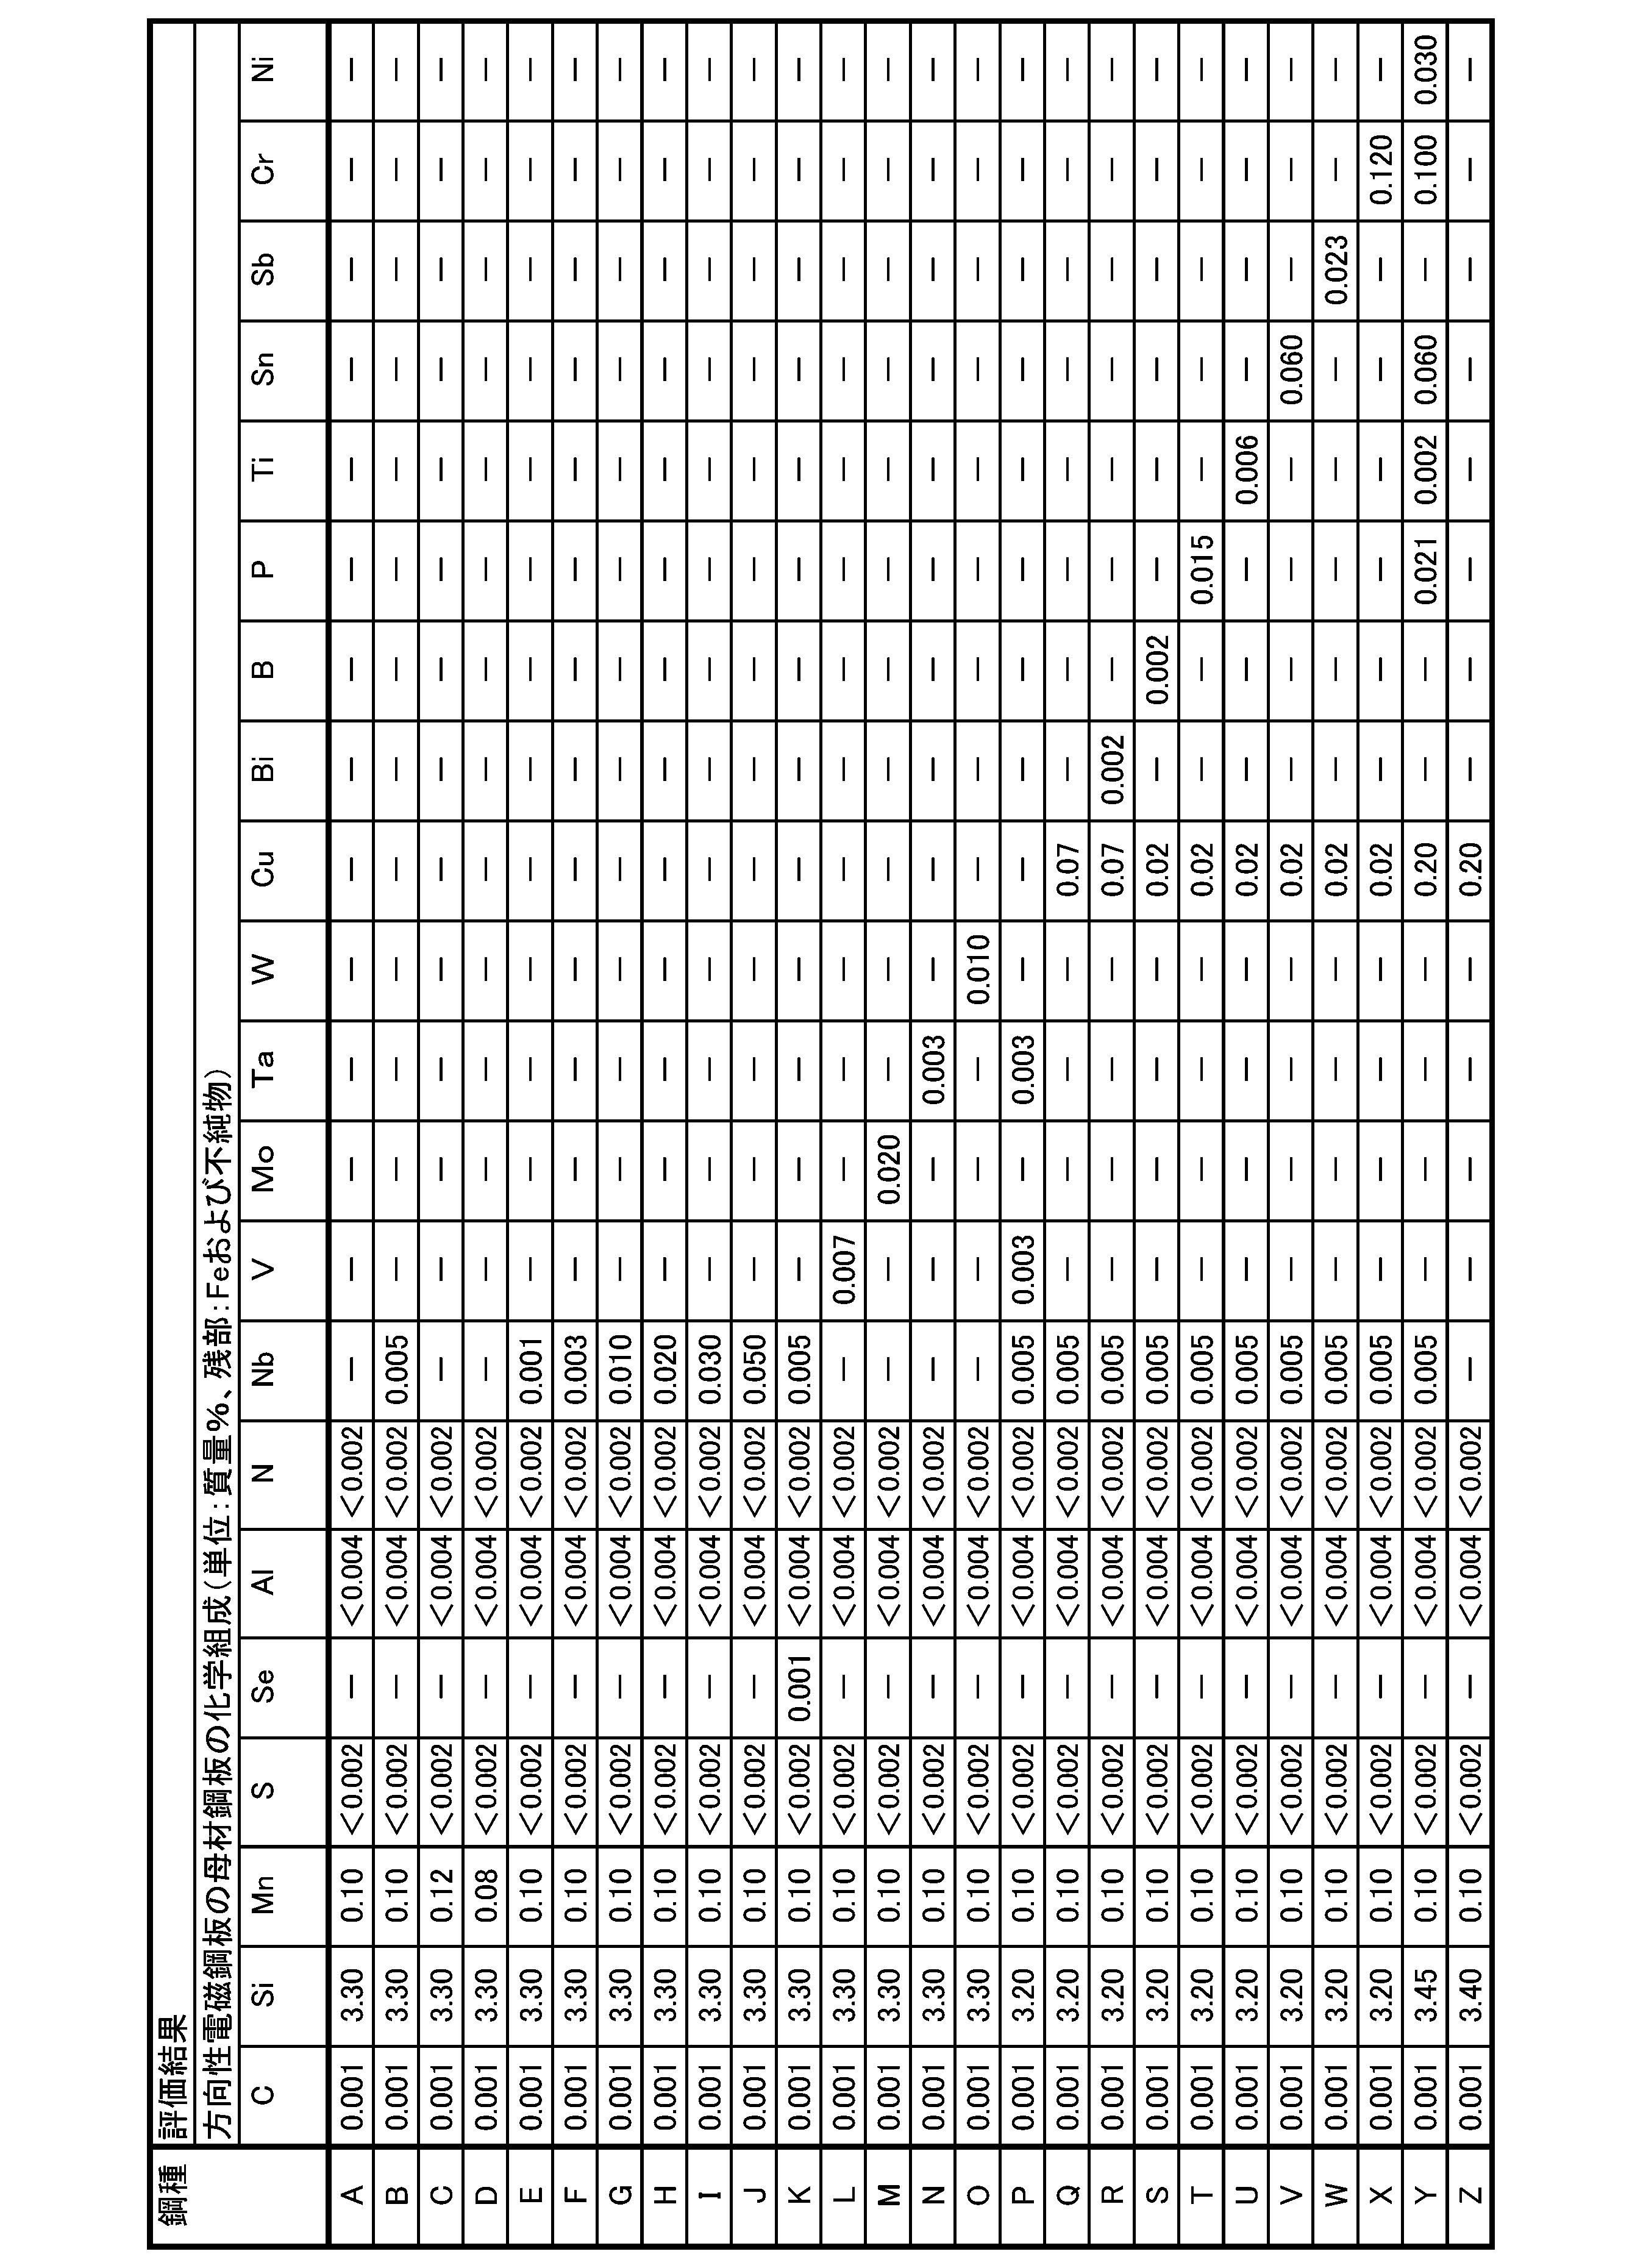
2 局所加熱影響領域
3 局所加熱非影響領域(マトリックス部)
4 局所加熱領域境界
5 局所加熱影響領域境界
14 ゴス方位粒
15 粗大ゴス方位粒
21 圧延方向
22 幅方向(圧延直角方向)
Claims (1)
- 母材鋼板と絶縁被膜とを有し且つ磁区制御された方向性電磁鋼板であって、
800A/mで励磁したときの圧延方向の磁束密度を単位:TでB8と定義し、
周波数50Hzで磁束密度1.7Tに励磁したときの鉄損を単位:W/kgでW17/50と定義し、
周波数50Hzで磁束密度1.7Tに励磁したときの磁歪波形のうちの200Hz成分の磁歪量から求める磁歪速度レベルを単位:dBでLva200@1.7Tと定義したとき、
前記B8が、B8≧1.940を満たし、
前記W17/50が、W17/50≦0.670を満たし、
前記Lva200@1.7Tが、Lva200@1.7T≦46.0を満たす
ことを特徴とする方向性電磁鋼板。
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020267001859A KR20260026554A (ko) | 2023-06-29 | 2024-06-27 | 방향성 전자 강판 |
| JP2025530188A JPWO2025005170A1 (ja) | 2023-06-29 | 2024-06-27 | |
| EP24832029.3A EP4737608A1 (en) | 2023-06-29 | 2024-06-27 | Grain-oriented electrical steel sheet |
| CN202480042002.9A CN121420087A (zh) | 2023-06-29 | 2024-06-27 | 取向性电磁钢板 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2023106861 | 2023-06-29 | ||
| JP2023-106861 | 2023-06-29 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2025005170A1 true WO2025005170A1 (ja) | 2025-01-02 |
Family
ID=93939108
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2024/023292 Ceased WO2025005170A1 (ja) | 2023-06-29 | 2024-06-27 | 方向性電磁鋼板 |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP4737608A1 (ja) |
| JP (1) | JPWO2025005170A1 (ja) |
| KR (1) | KR20260026554A (ja) |
| CN (1) | CN121420087A (ja) |
| WO (1) | WO2025005170A1 (ja) |
Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS572839A (en) | 1980-06-04 | 1982-01-08 | Nippon Steel Corp | Production of unidirectional silicon steel plate of high magnetic flux density |
| JPS61190017A (ja) | 1985-02-20 | 1986-08-23 | Nippon Steel Corp | 鉄損の低い一方向性珪素鋼板の製造方法 |
| JPH1187122A (ja) * | 1997-07-16 | 1999-03-30 | Nippon Steel Corp | 低騒音トランス用方向性電磁鋼板 |
| WO2004083465A1 (ja) | 2003-03-19 | 2004-09-30 | Nippon Steel Corporation | 磁気特性の優れた方向性電磁鋼板とその製造方法 |
| WO2016171129A1 (ja) | 2015-04-20 | 2016-10-27 | 新日鐵住金株式会社 | 方向性電磁鋼板 |
| JP2017128765A (ja) * | 2016-01-20 | 2017-07-27 | 新日鐵住金株式会社 | 方向性電磁鋼板、方向性電磁鋼板の製造方法、変圧器またはリアクトル用の鉄心、および、騒音評価方法 |
| JP2021123755A (ja) * | 2020-02-05 | 2021-08-30 | 日本製鉄株式会社 | 方向性電磁鋼板 |
| JP2022022483A (ja) * | 2020-06-24 | 2022-02-07 | 日本製鉄株式会社 | 方向性電磁鋼板の製造方法および方向性電磁鋼板 |
| CN114255971A (zh) * | 2020-09-22 | 2022-03-29 | 宝山钢铁股份有限公司 | 一种耐热刻痕取向硅钢及其刻痕方法 |
| JP2023106861A (ja) | 2022-01-21 | 2023-08-02 | 株式会社コナミアミューズメント | ゲームシステム、ゲームシステムの動作方法およびプログラム |
| WO2024063163A1 (ja) * | 2022-09-22 | 2024-03-28 | 日本製鉄株式会社 | 方向性電磁鋼板 |
-
2024
- 2024-06-27 JP JP2025530188A patent/JPWO2025005170A1/ja active Pending
- 2024-06-27 EP EP24832029.3A patent/EP4737608A1/en active Pending
- 2024-06-27 KR KR1020267001859A patent/KR20260026554A/ko active Pending
- 2024-06-27 WO PCT/JP2024/023292 patent/WO2025005170A1/ja not_active Ceased
- 2024-06-27 CN CN202480042002.9A patent/CN121420087A/zh active Pending
Patent Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS572839A (en) | 1980-06-04 | 1982-01-08 | Nippon Steel Corp | Production of unidirectional silicon steel plate of high magnetic flux density |
| JPS61190017A (ja) | 1985-02-20 | 1986-08-23 | Nippon Steel Corp | 鉄損の低い一方向性珪素鋼板の製造方法 |
| JPH1187122A (ja) * | 1997-07-16 | 1999-03-30 | Nippon Steel Corp | 低騒音トランス用方向性電磁鋼板 |
| WO2004083465A1 (ja) | 2003-03-19 | 2004-09-30 | Nippon Steel Corporation | 磁気特性の優れた方向性電磁鋼板とその製造方法 |
| WO2016171129A1 (ja) | 2015-04-20 | 2016-10-27 | 新日鐵住金株式会社 | 方向性電磁鋼板 |
| JP2017128765A (ja) * | 2016-01-20 | 2017-07-27 | 新日鐵住金株式会社 | 方向性電磁鋼板、方向性電磁鋼板の製造方法、変圧器またはリアクトル用の鉄心、および、騒音評価方法 |
| JP2021123755A (ja) * | 2020-02-05 | 2021-08-30 | 日本製鉄株式会社 | 方向性電磁鋼板 |
| JP2022022483A (ja) * | 2020-06-24 | 2022-02-07 | 日本製鉄株式会社 | 方向性電磁鋼板の製造方法および方向性電磁鋼板 |
| CN114255971A (zh) * | 2020-09-22 | 2022-03-29 | 宝山钢铁股份有限公司 | 一种耐热刻痕取向硅钢及其刻痕方法 |
| JP2023106861A (ja) | 2022-01-21 | 2023-08-02 | 株式会社コナミアミューズメント | ゲームシステム、ゲームシステムの動作方法およびプログラム |
| WO2024063163A1 (ja) * | 2022-09-22 | 2024-03-28 | 日本製鉄株式会社 | 方向性電磁鋼板 |
Also Published As
| Publication number | Publication date |
|---|---|
| CN121420087A (zh) | 2026-01-27 |
| KR20260026554A (ko) | 2026-02-26 |
| EP4737608A1 (en) | 2026-05-06 |
| JPWO2025005170A1 (ja) | 2025-01-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6319605B2 (ja) | 低鉄損方向性電磁鋼板の製造方法 | |
| JP6157360B2 (ja) | 方向性電磁鋼板およびその製造方法 | |
| CN105579596B (zh) | 取向性电磁钢板的制造方法 | |
| JP7606155B1 (ja) | 方向性電磁鋼板 | |
| JP7492112B2 (ja) | 方向性電磁鋼板 | |
| JP5691265B2 (ja) | 方向性電磁鋼板の製造方法 | |
| JP2012036445A (ja) | 方向性電磁鋼板およびその製造方法 | |
| KR20020013442A (ko) | 자속밀도가 높은 방향성 전자 강판의 제조 방법 | |
| JP5729014B2 (ja) | 方向性電磁鋼板の製造方法 | |
| JP7606154B1 (ja) | 方向性電磁鋼板 | |
| CN111417737A (zh) | 低铁损取向性电磁钢板及其制造方法 | |
| JP5923879B2 (ja) | 方向性電磁鋼板およびその製造方法 | |
| MX2012015155A (es) | Metodo para la produccion de chapa de acero magnetica de grano orientado. | |
| JP5594240B2 (ja) | 方向性電磁鋼板およびその製造方法 | |
| JPH06136449A (ja) | 低鉄損一方向性珪素鋼板の製造方法 | |
| WO2024214785A1 (ja) | 方向性電磁鋼板および方向性電磁鋼板の製造方法 | |
| JPH0768580B2 (ja) | 鉄損の優れた高磁束密度一方向性電磁鋼板 | |
| JP7787485B2 (ja) | 方向性電磁鋼板用の脱炭焼鈍鋼板 | |
| JP7640827B2 (ja) | 方向性電磁鋼板の製造方法および方向性電磁鋼板 | |
| KR20260026554A (ko) | 방향성 전자 강판 | |
| JPH05179355A (ja) | 低鉄損一方向性けい素鋼板の製造方法 | |
| WO2025005169A1 (ja) | 冷延鋼板 | |
| JPH02277780A (ja) | 低鉄損一方向性珪素鋼板及びその製造方法 | |
| JP7538460B1 (ja) | 鉄損特性に優れた方向性電磁鋼板 | |
| JPH0565543A (ja) | 歪取り焼鈍を施しても磁気特性の劣化がなくかつ幅方向に均一の特性を有する低鉄損一方向性珪素鋼板の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 24832029 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2025530188 Country of ref document: JP Kind code of ref document: A |
|
| REG | Reference to national code |
Ref country code: BR Ref legal event code: B01A Ref document number: 112025028666 Country of ref document: BR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202617001305 Country of ref document: IN |
|
| WWP | Wipo information: published in national office |
Ref document number: 202617001305 Country of ref document: IN |
|
| ENP | Entry into the national phase |
Ref document number: 1020267001859 Country of ref document: KR Free format text: ST27 STATUS EVENT CODE: A-0-1-A10-A15-NAP-PA0105 (AS PROVIDED BY THE NATIONAL OFFICE) |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1020267001859 Country of ref document: KR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2024832029 Country of ref document: EP Ref document number: 2026100854 Country of ref document: RU |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2024832029 Country of ref document: EP Effective date: 20260129 |
|
| ENP | Entry into the national phase |
Ref document number: 2024832029 Country of ref document: EP Effective date: 20260129 |
|
| WWP | Wipo information: published in national office |
Ref document number: 1020267001859 Country of ref document: KR |
|
| WWP | Wipo information: published in national office |
Ref document number: 2026100854 Country of ref document: RU |
|
| WWP | Wipo information: published in national office |
Ref document number: 2024832029 Country of ref document: EP |