WO2021171868A1 - 組立体、圧力測定用シートセット - Google Patents
組立体、圧力測定用シートセット Download PDFInfo
- Publication number
- WO2021171868A1 WO2021171868A1 PCT/JP2021/002553 JP2021002553W WO2021171868A1 WO 2021171868 A1 WO2021171868 A1 WO 2021171868A1 JP 2021002553 W JP2021002553 W JP 2021002553W WO 2021171868 A1 WO2021171868 A1 WO 2021171868A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- winding core
- sheet
- inner diameter
- layer
- assembly
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D85/00—Containers, packaging elements or packages, specially adapted for particular articles or materials
- B65D85/67—Containers, packaging elements or packages, specially adapted for particular articles or materials for web or tape-like material
- B65D85/671—Containers, packaging elements or packages, specially adapted for particular articles or materials for web or tape-like material wound in flat spiral form
- B65D85/672—Containers, packaging elements or packages, specially adapted for particular articles or materials for web or tape-like material wound in flat spiral form on cores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H75/00—Storing webs, tapes, or filamentary material, e.g. on reels
- B65H75/02—Cores, formers, supports, or holders for coiled, wound, or folded material, e.g. reels, spindles, bobbins, cop tubes, cans, mandrels or chucks
- B65H75/04—Kinds or types
- B65H75/08—Kinds or types of circular or polygonal cross-section
- B65H75/14—Kinds or types of circular or polygonal cross-section with two end flanges
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01L—MEASURING FORCE, STRESS, TORQUE, WORK, MECHANICAL POWER, MECHANICAL EFFICIENCY, OR FLUID PRESSURE
- G01L5/00—Apparatus for, or methods of, measuring force, work, mechanical power, or torque, specially adapted for specific purposes
Definitions
- the present invention relates to an assembly and a sheet set for pressure measurement.
- a sheet set for measuring pressure is known for measuring the distribution of pressure.
- the pressure measurement sheet set is composed of a sheet having a layer containing microcapsules containing a color former and a sheet having a layer containing a color developer. As described in Patent Document 1, the sheet is often transported and stored in a state of being wound around a winding core.
- the microcapsules are easily destroyed and do not function as a pressure measurement sheet.
- the present inventors have evaluated the characteristics of an assembly including a roll of a sheet obtained by winding a sheet having a layer containing microcapsules containing a color former in a winding core as described in Patent Document 1. It has been found that the microcapsules may be destroyed when an impact is applied due to a drop that is expected during transportation and handling.
- the present invention is an assembly having a sheet having a layer containing microcapsules containing a color-developing agent wound around a winding core, and even when an impact due to dropping is applied, the microcapsules are microscopic.
- An object of the present invention is to provide an assembly in which the destruction of the capsule is suppressed.
- Another object of the present invention is to provide a sheet set for pressure measurement.
- Winding core and A pair of flange members fixed to both ends of the winding core An assembly comprising a roll of a first sheet formed by winding a long first sheet having a first layer containing microcapsules containing a coloring agent on a winding core. An assembly in which the fixing strength between the winding core and the flange member is 20 N or more.
- the winding core has a hollow cylindrical shape.
- the flange member has a substrate and an insertion portion that can be inserted into the hollow portion of the winding core arranged on the substrate.
- the assembly according to (1), wherein the protrusion is arranged on the outer peripheral surface of the insertion portion.
- the assembly according to (2), wherein the number of protrusions is 3 or more.
- the change rate of the inner diameter of the winding core obtained by Test 1 described later is 1.0% or less.
- the diameter of the circumscribed circle circumscribing the region consisting of the insertion portion and the protrusion when observing the flange member from the normal direction of the substrate is 0.7 to 2.0 mm larger than the inner diameter of the winding core (2). )-(4).
- the assembly has a sheet having a layer containing microcapsules containing a color-developing agent wound around a winding core, and the microcapsules are destroyed even when an impact due to dropping is applied.
- An assembly that is restrained can be provided.
- FIG. 1 It is a perspective view which shows one Embodiment of the assembly of this invention. It is a perspective view which shows one Embodiment of a flange member. It is a top view of the flange member of FIG. It is a perspective view which shows the other embodiment of a flange member. It is sectional drawing which shows one Embodiment of 1st sheet. It is a top view of the first sheet of FIG.
- the numerical range represented by using "-" in the present specification means a range including the numerical values before and after "-" as the lower limit value and the upper limit value.
- the upper limit value or the lower limit value described in a certain numerical range may be replaced with the upper limit value or the lower limit value of another numerical range described stepwise. good.
- the upper limit value or the lower limit value described in a certain numerical range may be replaced with the value shown in the examples.
- Various components described later may be used alone or in combination of two or more.
- the polyisocyanate described later may be used alone or in combination of two or more.
- a feature of the assembly of the present invention is that the fixing strength between the winding core and the flange member is adjusted to a predetermined value or more.
- the present inventors since the solid strength between the winding core and the flange member is low, the present inventors tend to wobble between the winding core and the flange member during transportation and handling of the assembly, and the microcapsules It is probable that the microcapsules were easily destroyed as a result because the layer containing the above was susceptible to impact.
- the above-mentioned problem is suppressed by setting the above-mentioned fixing strength to a predetermined value or more.
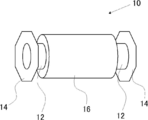
- FIG. 1 is a perspective view showing an embodiment of the assembly of the present invention.
- the assembly 10 is formed by winding a hollow cylindrical winding core 12, a pair of flange members 14 fixed to both ends of the winding core 12, and a long first sheet described later around the winding core 12. It has a roll 16 of the first sheet.
- FIG. 2 shows a perspective view of the flange member 14 shown in FIG.
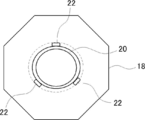
- FIG. 3 shows a top view of the flange member 14.
- the flange member 14 has a substrate (flange) 18, an insertion portion 20 arranged on the substrate 18, and a protrusion 22 arranged on the surface (outer peripheral surface) of the insertion portion 20.
- the insertion portion 20 of the flange member 14 can be inserted into the hollow portion of the hollow cylindrical winding core 12.
- the insertion portion 20 of the flange member 14 is inserted into the hollow portion of the winding core 12, and the protrusion 22 of the insertion portion 20 comes into contact with the inner peripheral surface of the winding core 12, so that the winding core 12 and the flange The member 14 is fixed.
- each member will be described in detail.
- the first sheet is wound around the winding core 12.
- the material of the winding core 12 include plastic, paper, wood, and metal. Among them, paper is preferable as the material of the winding core in that the fixing strength between the winding core and the flange member is 20 N or more. Examples of the paper include paper tube base paper and resin-impregnated paper.
- the pulp used as a raw material for paper may be virgin pulp such as chemical pulp and high-yield pulp, or recycled pulp.
- the size of the winding core 12 is not particularly limited, but the outer diameter (outer diameter of the winding core) is preferably 50 to 350 mm, more preferably 85 to 90 mm. When the winding core has a shape other than a cylindrical shape, the outer diameter corresponds to the diameter of the circumscribed circle of the winding core.
- the inner diameter of the cylindrical winding core 12 is preferably 45 to 345 mm, more preferably 70 to 85 mm.
- the inner diameter and the wall thickness (thickness corresponding to the difference between the outer diameter and the inner diameter) of the winding core 12 do not change depending on the environmental conditions.
- the inner diameter change rate of the winding core obtained by the following test 1 is preferably 1.0% or less
- the wall thickness change rate of the winding core obtained by the following test 2 is 10.0% or less. Is preferable.
- the lower limit of the inner diameter change rate and the wall thickness change rate is not particularly limited, but may be 0%.
- Test 1 After allowing the winding core to stand in an environment of 23 ° C. and 65% RH for 24 hours, the inner diameter of the winding core is measured at four points to obtain the inner diameter before heating, and then the winding core is 105.
- Rate of change ⁇
- Test 2 After allowing the winding core to stand for 24 hours in an environment of 23 ° C.
- the wall thickness of the winding core is measured at four places to obtain the wall thickness before heating, and then the winding core is obtained.
- the wall thickness of the winding core was measured at the above four places to obtain the wall thickness after heating, and the wall thickness was obtained at the above four places before heating.
- the rate of change obtained by the following formula (2) at the above four locations is calculated, and the obtained average value is further calculated and averaged to obtain a value.
- the rate of change in wall thickness. Equation (2): Rate of change ⁇
- the surface surface Ra of the outer peripheral surface of the winding core is not particularly limited, but is often 1.0 to 20 ⁇ m, and 1.0 to 4.0 ⁇ m is preferable in that damage to the first sheet can be further prevented. ..
- a stylus type surface roughness meter (Handy Surf E-35A, manufactured by Tokyo Seimitsu Co., Ltd.) is used, and the surface roughness (Ra) of the surface of the winding core is determined according to ISO97. To measure.
- the measurement conditions are an evaluation length of 4 mm and a cutoff value of 0.8 mm.
- the above measurement is carried out three times, and the obtained measured values are arithmetically averaged to obtain a surface roughness Ra.
- the winding core 12 has a hollow cylindrical shape in FIG. 1, the shape is not limited to the shape as long as the first sheet can be wound.
- the winding core may be a polygonal columnar shape.
- the winding core may be in a solid state.
- a cushion layer made of foamed polyethylene or the like may be provided between the winding core and the first sheet.
- the flange member 14 is fixed to both ends of the winding core 12. As described above, in FIG. 1, the winding core 12 and the flange member 14 are fixed by the protrusion 22 in the flange member 14 coming into contact with the inner peripheral surface of the winding core 12.
- Examples of the material of the flange member 14 include plastic, paper, wood, and metal. Of these, plastic is preferable. Examples of the plastic include polypropylene, polyethylene, and polyethylene terephthalate, and polypropylene is preferable.
- the insertion portion 20 and the protrusion 22 described later are also preferably made of the above materials.
- the flange member 14 includes a substrate 18.
- the substrate 18 has an octagonal shape, but the shape is not particularly limited, and may be a circular shape or a polygonal shape other than the octagonal shape (for example, a hexagonal shape). ..
- the thickness of the substrate 18 is not particularly limited, but is preferably 1 to 50 mm, more preferably 2 to 20 mm.
- the size of the substrate 18 is not particularly limited, but it is usually preferable that the size of the substrate 18 is larger than the outer diameter of the roll 16 of the first sheet.
- the size of the substrate 18 means the diameter of the circumscribed circle of the substrate 18.
- the size of the substrate 18 is preferably 1 mm or more larger than the roll 16 of the first sheet, and more preferably 5 mm or more.
- the upper limit is not particularly limited, but it is often 600 mm or less.
- the flange member 14 has an insertion portion 20 arranged on the substrate 18.
- the insertion portion 20 is a member extending along the normal direction of the substrate 18.
- the length of the insertion portion 20 along the extending direction is not particularly limited, but is preferably 2 to 100 mm, more preferably 20 to 30 mm.
- the insertion portion 20 shown in FIGS. 2 and 3 has a cylindrical shape, but is not limited to this form as long as it can be inserted into the hollow portion of the winding core 12.
- the shape of the insertion portion may be polygonal. ..
- the outer diameter of the insertion portion 20 (the outer diameter of the insertion portion 20) is preferably smaller than the inner diameter of the winding core 12.
- the outer diameter of the insertion portion 20 is preferably 45 to 345 mm, more preferably 70 to 85 mm.
- the normal direction of the substrate 18 is such that the destruction of the microcapsules is further suppressed even when an impact due to dropping is applied (hereinafter, also simply referred to as "a point where the effect of the present invention is more excellent").
- the diameter of the circumscribed circle (hereinafter, also simply referred to as “the diameter of the circumscribed circle”) circumscribed in the region consisting of the insertion portion 20 and the protrusion 22 when the flange member 14 is observed from the inside is 0 than the inner diameter of the winding core 12. It is preferably 7 to 2.0 mm larger.
- the circumscribed circle is a circle that circumscribes the region including the insertion portion 20 and the protrusion 22 when the flange member 14 is observed from the normal direction of the substrate 18, and is shown in FIG. It is represented by a broken line.
- a protrusion 22 is arranged on the outer peripheral surface of the insertion portion 20.
- the number of protrusions 22 is 3, but the number is not particularly limited and may be 4 or more.
- the number of protrusions 22 is preferably 3 or more, and more preferably 4 or more, in that the effect of the present invention is more excellent.
- the upper limit is not particularly limited, and in many cases, the number is 100 or less.
- the three protrusions 22 are arranged at equal intervals on the outer peripheral surface of the insertion portion 20.
- the arrangement position of the protrusions is not limited to the embodiment shown in FIG. 3, but when there are a plurality of protrusions, it is preferable that the plurality of protrusions are arranged at equal intervals on the outer peripheral surface of the insertion portion.
- the three protrusions 22 are arranged so as to be in contact with the substrate 18.
- the relationship between the distance between the protrusion and the substrate is not limited to the embodiment shown in FIG. 3, but it is preferable that the distance between the plurality of protrusions and the substrate is the same. That is, it is preferable that the distance between the protrusion and the substrate is the same in each protrusion.
- the shape of the protrusion 22 is rectangular, but the shape is not particularly limited.
- the height of the protrusion 22 (height from the outer peripheral surface of the insertion portion 20) is not particularly limited, and when the insertion portion 20 is inserted into the hollow portion of the winding core 12, the protrusion is projected on the inner peripheral surface of the winding core 12.
- the height is not particularly limited as long as the height is such that the portions 22 come into contact with each other. Among them, 0.1 to 5 mm is preferable, 0.5 to 2 mm is more preferable, and 0.5 to 1.5 mm is further preferable.
- the height of the protrusion may be constant or may differ depending on the position. For example, in that the effect of the present invention is more excellent, the height of the protrusion may be lowered toward the end of the protrusion in the direction orthogonal to the direction in which the protrusion extends.
- the width in the direction orthogonal to the extending direction of the protrusion 22 is not particularly limited, but is preferably 1 to 25 mm, more preferably 5 to 10 mm.
- the flange member is not limited to the form shown in FIGS. 2 and 3, and for example, as shown in FIG. 4, the substrate 180 included in the flange member 140 may be provided with a hole 40. By passing a finger through the hole 40, the assembly can be easily carried without dropping. In FIG. 4, eight holes 40 are provided, but the number thereof is not particularly limited and may be one or a plurality.
- the roll 16 of the first sheet is a wound product made of the first sheet, which is formed by winding the first sheet around the winding core.
- the first sheet has a long shape.
- the elongated shape means that the length in the longitudinal direction is longer than the length in the lateral direction.
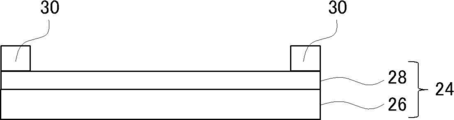
- FIG. 5 shows a cross-sectional view in the width direction of one embodiment of the first sheet
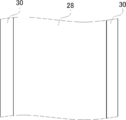
- FIG. 6 shows a top view of the first sheet of FIG.
- the first sheet 24 shown in FIGS. 5 and 6 has a support 26 and a first layer 28 arranged on the support 26.
- a pair of spacers 30 are arranged on the first sheet 24. As shown in FIGS.
- the pair of spacers 30 are arranged apart from each other in the width direction of the first sheet 24.
- the first sheet 24 in which the pair of spacers 30 is arranged is wound around the winding core, due to the presence of the spacers 30, the first layer 28 and the first layer 28 It is possible to suppress contact with the support 26 located on the side opposite to the winding core side, and it is possible to suppress the destruction of the microcapsules in the first layer 28. Therefore, it is preferable that the assembly further has a pair of spacers arranged between the first sheets of the rolls of the first sheet and spaced apart in the width direction of the first sheet. The specific configuration of the first sheet will be described in detail later.
- the material of the spacer 30 is not particularly limited, but a rubber foam or an elastic foam is preferable.
- the rubber foam include a rubber foam selected from the group consisting of natural rubber, isoprene rubber, styrene rubber, nitrile rubber, butadiene rubber, chloroprene rubber, and urethane rubber.
- the elastic foam include an elastic foam selected from the group consisting of polyethylene, polypropylene, polystyrene, polyvinyl chloride, and polyvinyl acetate.
- the thickness of the spacer 30 is not particularly limited, but is preferably thicker than that of the first layer 28.
- the thickness of the spacer 30 is often 1 to 10 mm, and is preferably 1 to 5 mm, more preferably 2.5 to 5 mm, in that the effect of the present invention is more excellent.
- the coefficient of static friction of the spacer 30 is not particularly limited, but is preferably 0.1 to 1.0 in that the effect of the present invention is more excellent.
- the coefficient of kinetic friction of the spacer 30 is not particularly limited, but is preferably 0.1 to 1.0 in that the effect of the present invention is more excellent.
- the method of arranging the spacer 30 on the first sheet 24 is not particularly limited, and examples thereof include a method of using double-sided tape and a method of using an adhesive or an adhesive.
- spacers 30 are provided over the entire longitudinal direction of the first sheet.
- the present invention is not limited to this form, and the spacer may be provided in a part of the first sheet in the longitudinal direction.
- the spacer 30 is arranged on the first sheet 24 shown in FIGS. 5 and 6, the present invention is not limited to this embodiment, and the assembly does not have to include the spacer.
- the rigidity of the first sheet in the width direction is not particularly limited, and is often 160 mN or more, and 170 mN or more is preferable, and 180 mN or more is more preferable in that the effect of the present invention is more excellent.
- the upper limit is not particularly limited, but in many cases it is 500 mN or less, preferably 300 mN or less.
- the rigidity of the first sheet in the longitudinal direction is not particularly limited, and is often 500 mN or less, and 200 mN or less is preferable, and 160 mN or less is preferable in that the effect of the present invention is more excellent.
- the lower limit is not particularly limited, but in many cases it is 50 mN or more, and 100 mN or more is preferable.
- the method for measuring the rigidity is as follows. From the first sheet, test pieces of 200 mm in the longitudinal direction (longitudinal direction) and 15 mm in the width direction (horizontal direction) were cut out, and using LOOP STIFFNESS TESTER (manufactured by Toyo Seiki Seisakusho), the cut out test pieces were cut out in the longitudinal direction and the width direction. Measure stiffness. The measurement conditions are a clamp interval distance of 100 mm, a loop length of 85 mm, and a compression speed of 3.3 mm / sec. Two samples are measured, and the average value is taken as the above-mentioned rigidity.
- the above measurement is performed on two test pieces, and the average value of the longitudinal rigidity obtained from the two test pieces is defined as the longitudinal rigidity of the first sheet, which is obtained from the two test pieces.
- the average value of the rigidity in the width direction is defined as the rigidity in the width direction of the first sheet.
- the insertion portion 20 of the flange member 14 is inserted into the hollow portion of the winding core 12 to fix both, but the fixing method is not limited to this embodiment. ..
- the fixing method is not limited to this embodiment. ..
- the winding core and the flange member may be fixed by the portion in contact with the flange member.
- a fixing method other than the method using the protrusion may be used.
- the winding core and the flange member may be adhered and fixed with an adhesive. Further, the winding core and the flange member may be screwed together.
- the fixing strength between the winding core and the flange member is 20 N or more, and 25 N or more is preferable, and 28 N or more is more preferable in that the effect of the present invention is more excellent.
- the upper limit is not particularly limited, but in many cases it is 1000 N or less, more often 500 N or less, and even more often 200 N or less.
- the fixing strength is the strength (N) required for separating the winding core and the flange member, and is calculated by the following method. When one flange member of the assembly is fixed and the other flange member is pulled away from the winding core along the direction in which the winding core direction extends, one flange member or the other flange member becomes the winding core.
- the strength (N) when separated from the above is defined as the above-mentioned fixed strength.
- a force gauge manufactured by IMADA, model number: ZTA-500N
- the method for adjusting the fixing strength is not particularly limited, and examples thereof include a method for increasing the number of protrusions described above and a method for adjusting the difference between the diameter of the circumscribed circle and the inner diameter of the winding core.
- the fixing strength of the assembly can be controlled by adjusting the material of the winding core. For example, when a hard winding core is used, the winding core is not easily deformed when the protrusion comes into contact with the inner wall of the winding core, so that the fixing strength tends to be high. On the other hand, when a soft winding core is used, when the protrusion comes into contact with the inner wall of the winding core, the winding core is deformed to relieve the pressure by the protrusion, so that the fixing strength tends to be low.
- the assembly of the present invention may be encapsulated in a package. It may be a bag, or it may be a container including a container body having an opening and a lid for closing the opening.
- the material constituting the package is not particularly limited, and examples thereof include resins, and more specifically, polyolefin resins, polyethylene resins, and polypropylene resins.
- the color of the package is not particularly limited, and examples thereof include transparent color, brown, and black. Among them, brown or black is preferable, and black is more preferable, in terms of light resistance.
- the assembly of the present invention may be combined with a second sheet having a second layer containing a color developer to form a sheet set for pressure measurement.
- the second sheet will be described in detail later.
- the second sheet may be treated as an assembly. That is, the pressure measurement sheet set of the present invention has a first layer including a winding core, a pair of flange members fixed to both ends of the winding core, and microcapsules wound around the winding core and containing a color former.
- the first sheet and the second sheet are laminated so that the first layer in the first sheet and the second layer in the second sheet face each other. ..
- the microcapsules are broken in the pressurized region, and the color-developing agent contained in the microcapsules comes out from the microcapsules, and the color-developing agent in the second layer is combined with the color-developing agent.
- the color reaction progresses between them. As a result, color development progresses in the pressurized region.
- the first sheet has a first layer containing microcapsules containing a color former.
- the first sheet preferably has a first support and a first layer arranged on the first support. In the following, each member will be described in detail.
- the first support is a member for supporting the first layer. If the first layer itself can be handled, the first sheet does not have to have the first support.
- the first support has an elongated shape.
- the elongated first support means a support whose length in the longitudinal direction is longer than the length in the lateral direction.
- the width of the first support is not particularly limited, but is often 50 to 1500 mm, preferably 50 to 500 mm.
- Examples of the first support include a resin film and synthetic paper.
- the resin film include a polyester film such as a polyethylene terephthalate film, a cellulose derivative film such as cellulose triacetate, a polyolefin film such as polypropylene and polyethylene, and a polystyrene film.
- Synthetic paper includes those obtained by biaxially stretching polypropylene or polyethylene terephthalate or the like to form a large number of microvoids (Yupo, etc.), those produced using synthetic fibers such as polyethylene, polypropylene, polyethylene terephthalate, and polyamide, and synthetic papers. Examples thereof include a part of paper, one side or both sides of which are laminated.
- a resin film or synthetic paper is preferable, and a resin film is more preferable, because the effect of the present invention is more excellent.
- the support is preferably transparent from the viewpoint that the color development property can be visually recognized even when the support is visually recognized from the support side.
- the thickness of the first support is preferably 10 to 200 ⁇ m from the viewpoint that the effect of the present invention is more excellent.
- the first layer contains microcapsules containing a color former.
- the materials constituting the microcapsules will be described in detail.
- Microcapsules generally have a core portion and a capsule wall for encapsulating a core material (encapsulated (also referred to as an encapsulated component)) forming the core portion.
- the microcapsules contain a color former as a core material (encapsulating component). Since the color-developing agent is encapsulated in the microcapsules, the color-developing agent can exist stably until the microcapsules are destroyed by pressure.
- the microcapsules have a capsule wall that encloses the core material.
- the material (wall material) for the capsule wall of the microcapsules include known resins conventionally used as the wall material for microcapsules containing a color former in the use of pressure-sensitive copying paper or thermal recording paper.
- Specific examples of the resin include polyurethane, polyurea, polyurethane urea, melamine-formaldehyde resin, and gelatin.
- the capsule wall of the microcapsules contains at least one resin selected from the group consisting of polyurethane urea, polyurethane, and polyurea.
- the capsule wall of the microcapsules is substantially made of resin. Being substantially composed of resin means that the content of the resin is 90% by mass or more with respect to the total mass of the capsule wall, and 100% by mass is preferable. That is, the capsule wall of the microcapsules is preferably made of resin.
- the polyurethane is a polymer having a plurality of urethane bonds, and is preferably a reaction product formed from a raw material containing a polyol and a polyisocyanate.
- the polyurea is a polymer having a plurality of urea bonds, and is preferably a reaction product formed from a raw material containing a polyamine and a polyisocyanate.
- the polyurethane urea is a polymer having a urethane bond and a urea bond, and is preferably a reaction product formed from a raw material containing a polyol, a polyamine, and a polyisocyanate.
- a part of the polyisocyanate reacts with water to form a polyamine, and as a result, polyurethane urea may be obtained.
- the melamine-formaldehyde resin is preferably a reaction product formed from polycondensation of melamine and formaldehyde.
- the polyisocyanate is a compound having two or more isocyanate groups, and examples thereof include aromatic polyisocyanates and aliphatic polyisocyanates.
- the polyisocyanate may be, for example, an adduct of a polyol such as trimethylolpropane and a bifunctional polyisocyanate.
- the polyol is a compound having two or more hydroxyl groups.
- a low molecular weight polyol eg, an aliphatic polyol or an aromatic polyol.
- a “low molecular weight polyol” has a molecular weight of 400 or less.
- Polyols are intended), polyvinyl alcohols, polyether polyols, polyester polyols, polylactone-based polyols, castor oil-based polyols, polyolefin-based polyols, and hydroxyl group-containing amine-based compounds (for example, amino alcohols.
- hydroxyl group-containing amine-based compounds for example, amino alcohols.
- examples thereof include propylene oxide of an amino compound such as ethylenediamine or an ethyleneoxide adduct, such as N, N, N', N'-tetrax [2-hydroxypropyl] ethylenediamine, etc.).
- the polyamine is a compound having two or more amino groups (primary amino group or secondary amino group), and is, for example, diethylenetriamine, triethylenetetramine, 1,3-propylenediamine, and hexa.
- Aliphatic polyvalent amines such as methylenediamine; epoxy compound adducts of aliphatic polyvalent amines; alicyclic polyvalent amines such as piperazine; 3,9-bis-aminopropyl-2,4,8,10-tetraoxa Examples thereof include heterocyclic diamines such as Spiro- (5,5) undecane.
- the glass transition temperature of the capsule wall of the microcapsule is not particularly limited, but is preferably 50 to 160 ° C, more preferably 80 to 150 ° C.
- the method for measuring the glass transition temperature of the capsule wall is as follows. Fifty first layers (microcapsule layers) having a length of 1 cm and a width of 1 cm are prepared, and all of them are immersed in 10 ml of water and allowed to stand for 24 hours to obtain an aqueous dispersion of microcapsules. When the first sheet includes the first support, 50 sheets of 1 cm in length ⁇ 1 cm in width may be prepared and immersed in the first sheet. The obtained aqueous dispersion of microcapsules is centrifuged at 15,000 rpm for 30 minutes, and the microcapsules are separated.
- Ethyl acetate is added to the separated microcapsules, and the mixture is further stirred at 25 ° C. for 24 hours. Then, the obtained solution is filtered, and the obtained residue is vacuum-dried at 60 ° C. for 48 hours to obtain microcapsules containing nothing inside (hereinafter, also simply referred to as “measurement material”). Be done. That is, a capsule wall material of microcapsules, which is a measurement target of the glass transition temperature, can be obtained. Next, the thermal decomposition temperature of the obtained measurement material is measured using a thermogravimetric differential thermal analyzer TG-DTA (device name: DTG-60, Shimadzu Corporation).
- TG-DTA thermogravimetric differential thermal analyzer
- the thermal decomposition temperature refers to the temperature of the measurement material raised from room temperature at a constant temperature rise rate (10 ° C./min) with respect to the mass of the measurement material before heating. The temperature at which the weight is reduced by 5% by mass is defined as the thermal decomposition temperature (° C.).
- the glass transition temperature of the measurement material was measured using a differential scanning calorimeter DSC (device name: DSC-60a Plus, Shimadzu Corporation) using a closed pan, and the temperature rise rate was 25 ° C./min. Measure in the range of ° C to (pyrolysis temperature (° C) -5 ° C). As the glass transition temperature of the capsule wall of the microcapsule, the value at the time of raising the temperature in the second cycle is used.
- the average particle size of the microcapsules is not particularly limited, but is preferably 1 to 80 ⁇ m, more preferably 5 to 70 ⁇ m, and even more preferably 10 to 50 ⁇ m in terms of volume-based median diameter (D50).
- the median diameter based on the volume of the microcapsules can be controlled by adjusting the manufacturing conditions of the microcapsules and the like.
- the volume-based median diameter of the microcapsules is the volume of the particles on the large diameter side and the small diameter side when the entire microcapsule is divided into two with the particle diameter at which the cumulative volume is 50% as a threshold. The diameter at which the total is equal. That is, the median diameter corresponds to the so-called D50.
- the average wall thickness of the number of microcapsules (the average wall thickness of the number of capsule walls of the microcapsules) is not particularly limited, but is preferably 0.01 ⁇ m or more and 2 ⁇ m or less, more preferably more than 0.02 ⁇ m and less than 2 ⁇ m, and 0.05 ⁇ m or more. 5 ⁇ m or less is more preferable.
- the wall thickness of the microcapsules refers to the thickness ( ⁇ m) of the capsule wall forming the capsule particles of the microcapsules, and the number average wall thickness is the thickness ( ⁇ m) of the individual capsule walls of the five microcapsules. Is obtained by a scanning electron microscope (SEM) and averaged.
- a cross-sectional section of the first sheet containing the first layer containing microcapsules was prepared, and the cross section was observed at 200 times by SEM (value of average particle size of microcapsules) ⁇ 0.
- SEM value of average particle size of microcapsules
- the major axis means the longest diameter when observing the microcapsules.
- the ratio ( ⁇ / Dm) of the number average wall thickness ⁇ of the microcapsules to the average particle size Dm of the microcapsules is not particularly limited, and is often 0.001 or more. Above all, it is preferable to satisfy the relationship of the formula (1) in that the effect of the present invention is more excellent. Equation (1) 0.100> ⁇ / Dm> 0.001 That is, the above ratio ( ⁇ / Dm) is preferably larger than 0.001 and less than 0.100. When the relationship of the equation (1) is satisfied, the color density gradation can be easily recognized according to the pressure.
- a color former is encapsulated in the microcapsules.
- a color former is a compound that develops a color when it comes into contact with a color developer described later from a colorless state.
- an electron-donating dye precursor precursor of a dye that develops color
- the color former an electron-donating colorless dye is preferable.
- the color former those known in the application of pressure-sensitive copying paper or thermal recording paper can be used.
- Examples of the color former include triphenylmethanephthalide compounds, fluorene compounds, phenothiazine compounds, indolylphthalide compounds, azaindrillphthalide compounds, leucooramine compounds, rhodamine lactam compounds, and tris. Examples thereof include phenylmethane-based compounds, diphenylmethane-based compounds, triazene-based compounds, spiropyran-based compounds, and fluorene-based compounds. Examples of the above compounds include the compounds described in JP-A-5-257272, the compounds described in paragraphs 0030 to 0033 of International Publication No. 2009/8248, and 3', 6'-bis (diethylamino) -2- (4).
- the molecular weight of the color former is not particularly limited, and is preferably 300 or more.
- the upper limit is not particularly limited, but is preferably 1000 or less.
- microcapsules may contain components other than the above-mentioned color former.
- microcapsules preferably contain a solvent.
- the solvent is not particularly limited, and for example, an alkylnaphthalene compound such as diisopropylnaphthalene, a diarylalkane compound such as 1-phenyl-1-xsilylethane, an alkylbiphenyl compound such as isopropylbiphenyl, a triarylmethane compound, and an alkylbenzene compound.
- Aromatic hydrocarbons such as benzylnaphthalene compounds, diarylalkylene compounds, and arylindane compounds; aliphatic hydrocarbons such as dibutyl phthalate and isoparaffin; soybean oil, corn oil, cottonseed oil, rapeseed oil, olive oil, Examples thereof include natural animal and vegetable oils such as coconut oil, castor oil, and fish oil, and high-boiling distillates of natural compounds such as mineral oil.
- the mass ratio of the solvent to the color former is preferably in the range of 98/2 to 30/70 in terms of color development.
- the range of 97/3 to 40/60 is more preferable.
- the microcapsules may contain one or more additives such as an ultraviolet absorber, a light stabilizer, an antioxidant, a wax, and an odor suppressant, if necessary.
- additives such as an ultraviolet absorber, a light stabilizer, an antioxidant, a wax, and an odor suppressant, if necessary.
- the method for producing microcapsules is not particularly limited, and examples thereof include known methods such as an interfacial polymerization method, an internal polymerization method, a phase separation method, an external polymerization method, and a core selvation method. Of these, the interfacial polymerization method is preferable.
- the interfacial polymerization method will be described by taking as an example a method for producing microcapsules in which the capsule wall is polyurea or polyurethane urea.
- the interfacial polymerization method is a raw material containing a color former, a solvent having a boiling point of 100 ° C.
- a capsule wall material for example, polyisocyanate and at least one selected from the group consisting of polyols and polyamines.
- a polyamine is produced in a system by reacting isocyanate with water, a polyol and a polyamine may not be used.
- Interfacial weight including (emulsification step) and step of polymerizing the capsule wall material at the interface between the oil phase and the aqueous phase to form a capsule wall to form microcapsules containing a color former (encapsulation step).
- Legal is preferred.
- the mass ratio of the total amount of polyol and polyamine to the amount of polyisocyanate (total amount of polyol and polyamine / amount of polyisocyanate) in the above raw materials is not particularly limited, but is 0.1 / 99.9 to. 30/70 is preferable, and 1/99 to 25/75 is more preferable.
- the type of emulsifier used in the emulsification step is not particularly limited, and examples thereof include a dispersant and a surfactant.
- examples of the dispersant include polyvinyl alcohol.
- the first layer may contain other components (for example, binder, surfactant) in addition to the above-mentioned microcapsules.
- the mass (g / m 2 ) per unit area of the first layer is not particularly limited, but 0.5 to 30 g / m 2 is preferable because the effect of the present invention is more excellent.
- the method for forming the first layer is not particularly limited. For example, a method of applying a composition for forming a first layer containing microcapsules on a first support and heat-treating the obtained coating film at a predetermined temperature or higher can be mentioned. In addition to the above, there is also a method in which microcapsules are separately prepared and a composition for forming a first layer containing the microcapsules is applied onto the first support. In the following, a mode of heating at a predetermined temperature or higher will be described in detail.
- the composition for forming the first layer preferably contains at least microcapsules and a solvent.
- the microcapsule dispersion obtained by the above-mentioned interfacial polymerization method may be used as the composition for forming the first layer.
- the composition for forming the first layer may contain other components that may be contained in the first layer described above.
- the method of applying the composition for forming the first layer is not particularly limited, and examples of the coating machine used at the time of application include an air knife coater, a rod coater, a bar coater, a curtain coater, a gravure coater, and an extrusion coater. , Die coater, slide bead coater, and blade coater.
- the obtained coating film is heat-treated at a predetermined temperature or higher.
- the optimum temperature is selected according to the material of the capsule wall of the microcapsules used, but 60 ° C. or higher is preferable, and 70 ° C. or higher is preferable because the effect of the present invention is more excellent. More preferred.
- the upper limit is not particularly limited, but it is often 180 ° C. or lower, and 140 ° C. or lower is preferable, and 120 ° C. or lower is more preferable in that the color development density is more excellent.
- the heating time is not particularly limited, but 1.0 to 20 minutes is preferable, and 3.0 to 10 minutes is more preferable, from the viewpoint of more excellent effect of the present invention and productivity.
- the method of forming the first layer on the first support is not limited to the above embodiment.
- the temporary support is peeled off.
- the first sheet composed of the first layer may be formed.
- the temporary support is not particularly limited as long as it is a peelable support.
- the first sheet may have members other than the first support and the first layer described above.
- the first sheet may have an easy-adhesion layer between the first support and the first layer to enhance the adhesion between the first support and the first layer.
- the thickness of the easy-adhesion layer is not particularly limited, and is preferably 0.005 to 2 ⁇ m, more preferably 0.01 to 1 ⁇ m.
- the arithmetic mean roughness Ra of the first sheet is not particularly limited, and is often 0.1 ⁇ m or more, and is preferably 2.5 to 7.0 ⁇ m in that the color density is more excellent.
- the arithmetic mean roughness Ra of the first sheet is intended to be the arithmetic average roughness Ra of the surface of the first sheet facing the second sheet (contacting side) when using the pressure measurement sheet set. do.
- the arithmetic mean roughness Ra is the arithmetic mean roughness of the surface of the first layer opposite to the first support side. It corresponds to Ra.
- the arithmetic mean roughness Ra in the present specification (the arithmetic average roughness Ra on the first sheet and the arithmetic average roughness Ra on the second sheet described later) is the arithmetic defined in JIS B 0681-6: 2014. It means the average roughness Ra.
- a scanning white interferometer using an optical interferometry method (specifically, NewView 5020 manufactured by Zygo; objective lens ⁇ 50 times; intermediate lens ⁇ 0.5 times) is used.
- the measurement mode when measuring the arithmetic mean roughness Ra of the first sheet using the scanning white interferometer is the Stich mode
- the measurement mode when measuring the arithmetic mean roughness Ra of the second sheet is the Micro mode. Is.
- the second sheet has a second layer containing a color developer.
- the second sheet preferably includes a second support and a second layer arranged on the second support. In the following, each member will be described in detail.
- the second support is a member for supporting the second layer. If the second layer itself can be handled, the second sheet does not have to have the second support.
- the mode of the second support is not particularly limited, and examples thereof include the mode of the first support described above.
- the second layer is a layer containing a color developer.
- the color developer is a compound that does not have a color-developing function by itself, but has a property of causing the color-developing agent to develop color when it comes into contact with the color-developing agent.
- an electron-accepting compound is preferable.
- the color developer include inorganic compounds and organic compounds, and the inorganic compounds and organic compounds described in paragraphs 0055 to 0056 of International Publication No. 2009/008248 are preferable. Acidic clay, activated clay, or a metal salt of an aromatic carboxylic acid is preferable in that the color density and the image quality after color development are more excellent.
- the content of the color developer in the second layer is not particularly limited, but is preferably 20 to 95% by mass and more preferably 30 to 90% by mass with respect to the total mass of the second layer in that the color development concentration is more excellent. ..
- the content of the color developer in the second layer is not particularly limited, but is preferably 0.1 to 30 g / m 2.
- the content of the developer is preferably 3 to 20 g / m 2 and more preferably 5 to 15 g / m 2 .
- the content of the developer is preferably 0.1 to 5 g / m 2 , more preferably 0.2 to 3 g / m 2 .
- the second layer may contain components other than the above-mentioned developer.
- Other components include, for example, polymer binders, pigments, optical brighteners, defoamers, penetrants, UV absorbers, surfactants, and preservatives.
- the polymer binder include styrene-butadiene copolymer, polyvinyl acetate, polyacrylic acid ester, polyvinyl alcohol, polyacrylic acid, maleic anhydride-styrene copolymer, olefin resin, and modified acrylic acid ester copolymer.
- the pigment include heavy calcium carbonate, light calcium carbonate, talc, titanium dioxide and the like.
- the thickness of the second layer is not particularly limited, but 1 to 50 ⁇ m is preferable, and 2 to 30 ⁇ m is more preferable, because the effect of the present invention is more excellent.
- the mass (g / m 2 ) per unit area of the second layer is not particularly limited, but 0.5 to 30 g / m 2 is preferable because the effect of the present invention is more excellent.
- the method for forming the second layer is not particularly limited.
- a method of applying a composition for forming a second layer containing a color developer on a second support and, if necessary, subjecting the obtained coating film to a drying treatment can be mentioned.
- the composition for forming the second layer may be a dispersion liquid in which a color developer is dispersed in water or the like.
- the dispersion liquid in which the developer is dispersed can be prepared by mechanically dispersing the inorganic compound in water.
- the color developer is an organic compound, it can be prepared by mechanically dispersing the organic compound in water or dissolving it in an organic solvent.
- the composition for forming the second layer may contain other components that may be contained in the second layer described above.
- the method for applying the composition for forming the second layer is not particularly limited, and examples thereof include a method using a coating machine used for applying the composition for forming the first layer described above.
- the coating film may be subjected to a drying treatment, if necessary.
- a drying treatment include heat treatment.
- the method of forming the second layer on the second support is not limited to the above embodiment.
- the temporary support is peeled off.
- a second sheet composed of the second layer may be formed.
- the temporary support is not particularly limited as long as it is a peelable support.
- the second sheet may have members other than the above-mentioned second support and the second layer.
- the second sheet may have an easy-adhesion layer between the second support and the second layer to improve the adhesion between the two.
- the easy-adhesive layer include the easy-adhesive layer that the first sheet described above may have.
- the first sheet and the second sheet are laminated by laminating the first sheet and the second sheet so that the first layer of the first sheet and the second layer of the second sheet face each other. It is used by obtaining a body and pressurizing the laminate.
- the arithmetic mean roughness Ra of the second sheet is preferably 1.2 ⁇ m or less in that the color density is more excellent.
- the arithmetic mean roughness Ra of the second sheet is intended to be the arithmetic average roughness Ra of the surface of the second sheet facing the first sheet (contacting side) when using the pressure measurement sheet set. do.
- the arithmetic mean roughness Ra is the arithmetic mean roughness of the surface of the second layer opposite to the second support side. It corresponds to Ra.
- Example 1 As a coloring agent, 3,3-bis (2-methyl-1-octyl-3-indrill) phthalide (18 parts by mass) was dissolved in diarylethane (70 parts by mass) to obtain Solution A. Further, a butylene oxide adduct (0.4 parts by mass) of ethylenediamine dissolved in methyl ethyl ketone (1 part by mass) was added to the stirring solution A to obtain a solution B. Further, a trimethylolpropane adduct (2 parts by mass) of tolylene diisocyanate dissolved in methyl ethyl ketone (1 part by mass) was added to the stirring solution B to obtain a solution C.
- the above solution C was added to a solution in which polyvinyl alcohol (6 parts by mass) was dissolved in water (150 parts by mass), and the solution was emulsified and dispersed.
- Water (300 parts by mass) was added to the emulsion after emulsification and dispersion, and the mixture was heated to 70 ° C. with stirring, stirred for 1 hour and then cooled to prepare a microcapsule solution containing microcapsules containing a color former. ..
- the average particle size of the obtained microcapsules was 20 ⁇ m.
- the prepared microcapsule liquid was used as a color former-encapsulating microcapsule liquid (A).
- a coating liquid containing styrene-butadiene copolymer latex was applied to one side of a long polyethylene terephthalate (PET) film having a width of 450 mm and a thickness of 75 ⁇ m, and dried.
- PET polyethylene terephthalate
- a coating liquid containing gelatin and tin oxide was applied and dried to prepare a PET film 1 having an easy-adhesion layer having a thickness of 0.55 ⁇ m.
- the color-developing agent-encapsulating microcapsule solution (A) and the composition for forming a protective ear layer After applying the color-developing agent-encapsulating microcapsule solution (A) and the composition for forming a protective ear layer, the mixture was dried to obtain a sheet.
- the width of the first layer was 400 mm
- the width of the protective ear layer was 25 mm on one side (50 mm on both sides).
- the central portion of the sheet was cut to a width of 360 mm using a processing machine so as to remove the protective ear layers located at both ends in the width direction of the obtained sheet, and placed on the PCT film 1 and the PET film 1.
- a long first sheet having the first layer was obtained.
- the following double-sided tape is attached to both end edges in the width direction on the obtained first sheet, the following cushion (spacer) is attached, and spacers are arranged in the entire area in the longitudinal direction as shown in FIGS. 5 and 6.
- the first sheet was prepared.
- a hollow cylindrical winding core described later and a flange member described later were prepared.
- the flange member had a substrate and a cylindrical insertion portion arranged on the substrate, and a protrusion was arranged on the surface of the insertion portion (see FIGS. 2 and 3).
- the insertion portion of the flange member was inserted into the hollow portion of the winding core, and the flange members were fixed to both ends of the winding core to prepare a winding core with a flange member.
- the first sheet on which the spacer is arranged is wound around the winding core of the winding core with a flange member, and the assembly 1 as shown in FIG. 1 having a cross-sectional diameter (outer diameter of the roll of the first sheet) at both ends is 170 mm.
- a cross-sectional diameter outer diameter of the roll of the first sheet
- Neoprene foam rubber manufactured by Tokiwa Rubber Co., Ltd.
- Width 15 mm
- Thickness 5 mm
- Static friction coefficient 0.63
- Dynamic friction coefficient 0.62 -Double-sided tape- Japanese paper + acrylic adhesive (Sekisui Chemical Co., Ltd., double tack tape # 595)
- width 10 mm -Winding core- Made of paper (impregnated with resin)
- length 390 mm
- inner diameter of hollow part 76 mm -Flange member (see Fig.
- Example 1 Assemblies 2 to 12 were produced according to the same procedure as in Example 1 except that various requirements shown in Table 1 described later were changed. Further, also in Comparative Example 1, an assembly C1 was produced using a flange member having no protrusion. The inner diameter deformation rate, the wall thickness deformation rate, and the surface surface Ra of the winding core were adjusted by changing the type of the winding core used. The rigidity of the first sheet was adjusted by changing the type of PET film used.
- 1% aqueous solution (80 parts by mass) of sodium carboxymethyl cellulose (Daiichi Kogyo Seiyaku, Cellogen EP), 15% aqueous solution (18 parts by mass) of Na alkylbenzene sulfonate (Daiichi Kogyo Seiyaku, Neogen T), 1% aqueous solution (20 parts by mass) of polyoxyethylene polyoxypropylene lauryl ether (Daiichi Kogyo Seiyaku, Neugen LP-70), sodium-bis (3,3,4,4,5,5,6,6) , 6-Nonafluorohexyl) -2-Sulfinatooxysuccinate (Fujifilm, W-AHE) 1% aqueous solution (20 parts by mass) is mixed to prepare a composition for forming a second layer containing a clay substance.
- the composition for forming the second layer was applied onto a PET sheet having a thickness of 75 ⁇ m so that the amount of solid content applied was 7 g / m 2. Then, the obtained coating film was dried to form a second layer, and a second sheet was obtained.
- Example 11 a winding core made of a harder material than that of Examples 1 to 10, 12, and Comparative Example 1 was used.
- the surface roughness (Ra) of the surface of the winding core was measured according to ISO97 using a stylus type surface roughness meter (Handy Surf E-35A, manufactured by Tokyo Seimitsu Co., Ltd.). The measurement conditions were an evaluation length of 4 mm and a cutoff value of 0.8 mm. The above measurement was carried out three times, and the obtained measured values were arithmetically averaged to obtain surface roughness.
- the above measurement is performed on two test pieces, and the average value of the longitudinal rigidity obtained from the two test pieces is defined as the longitudinal rigidity of the first sheet, which is obtained from the two test pieces.
- the average value of the rigidity in the width direction was taken as the rigidity in the width direction of the first sheet.
- the first sheet included in each assembly and the second sheet cut into a size of 5 cm in length ⁇ 5 cm in width are arranged so that the surface of the first layer of the first sheet and the surface of the second layer of the second sheet face each other.
- the sheets were overlapped and pressed with a pressure press machine (DSF-C1-A, manufactured by Aida Engineering Co., Ltd.) at a pressure of 0.5 MPa to develop a color.
- DSF-C1-A manufactured by Aida Engineering Co., Ltd.
- both of the overlapped sheets were peeled off, and the density (DA) of the color-developing portion formed on the second sheet was measured using a densitometer RD-19 (manufactured by Gretag Macbeth).
- the initial concentration (DB) of the unused second sheet was measured by the same method.
- the "difference” column corresponds to the difference between the diameter of the circumscribed circle and the inner diameter of the winding core (diameter of the circumscribed circle and-inner diameter of the winding core).
- Example 3 As shown in Table 1, when the assembly of the present invention was used, the desired effect was obtained. Among them, it was confirmed from the comparison between Example 3 and other Examples that a more excellent effect was obtained when the number of protrusions was 4 or more. Further, from a comparison between Example 6 and other Examples, it was confirmed that a more excellent effect can be obtained when the thickness of the spacer is 2.5 ⁇ m or more. Further, from a comparison between Example 9 and other Examples, it was confirmed that a more excellent effect can be obtained when the rigidity of the first sheet in the width direction (lateral direction) is 170 mN or more.
- Example 13 N, N, N', N'-tetrakis (2-hydroxypropyl) ethylenediamine dissolved in synthetic isoparaffin (Idemitsu Kosan Co., Ltd., IP solvent 1620) (15 parts by mass), ethyl acetate (3 parts by mass) ) Adeca, Adecapolyether EDP-300) (0.4 parts by mass) is added to agitated 1-phenyl-1-xylylethane (Shin Nihon Petroleum Co., Ltd., Hysol SAS296) (78 parts by mass) to a solution. I got D.
- a trimethylolpropane adduct (DIC Corporation, Burnock D-750) (3 parts by mass) of trimethylolpropane dissolved in ethyl acetate (7 parts by mass) is added to the stirring solution D to prepare a solution. E was obtained. Then, the above solution E was added to a solution in which polyvinyl alcohol (PVA-205, Kuraray Co., Ltd.) (69 parts by mass) was dissolved in water (140 parts by mass), and the mixture was emulsified and dispersed. Water (340 parts by mass) was added to the emulsion after emulsification and dispersion, and the mixture was heated to 70 ° C. with stirring, stirred for 1 hour, and then cooled. Further, water was added to adjust the concentration to obtain a color former-free microcapsule solution (B) having a solid content concentration of 19.6%.
- Color-developing agent-encapsulating microcapsule solution (A) (18 parts by mass), color-developing non-encapsulating microcapsule solution (B) (2 parts by mass), water (63 parts by mass), colloidal silica (Nissan Kagaku Co., Ltd.) , Snowtex (registered trademark) 30) (1.8 parts by mass), 10% aqueous solution (1.8 parts by mass) of carboxymethyl cellulose Na (Daiichi Kogyo Seiyaku Co., Ltd., cellogen 5A), carboxymethyl cellulose Na (first) 1% aqueous solution (30 parts by mass) of Kogyo Seiyaku Co., Ltd., Cellogen EP), 15% aqueous solution (0.3 parts by mass) of sodium alkylbenzene sulfonate (Daiichi Kogyo Seiyaku Co., Ltd., Neogen T), and Neugen.
- a 1% aqueous solution (0.8 parts by mass) of LP70 (Daiichi Kogyo
- the assembly 13 was prepared according to the same procedure as the above ⁇ Preparation of the assembly B> except that the specific composition was used instead of the color former-encapsulating microcapsule solution (A).
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Storage Of Web-Like Or Filamentary Materials (AREA)
- Force Measurement Appropriate To Specific Purposes (AREA)
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2022503173A JP7360533B2 (ja) | 2020-02-25 | 2021-01-26 | 組立体、圧力測定用シートセット |
| CN202180013429.2A CN117279850A (zh) | 2020-02-25 | 2021-01-26 | 组件、压力测量用片材组 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2020-029519 | 2020-02-25 | ||
| JP2020029519 | 2020-02-25 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2021171868A1 true WO2021171868A1 (ja) | 2021-09-02 |
Family
ID=77490915
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2021/002553 Ceased WO2021171868A1 (ja) | 2020-02-25 | 2021-01-26 | 組立体、圧力測定用シートセット |
Country Status (4)
| Country | Link |
|---|---|
| JP (1) | JP7360533B2 (cg-RX-API-DMAC7.html) |
| CN (1) | CN117279850A (cg-RX-API-DMAC7.html) |
| TW (1) | TWI867157B (cg-RX-API-DMAC7.html) |
| WO (1) | WO2021171868A1 (cg-RX-API-DMAC7.html) |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH11240676A (ja) * | 1997-12-22 | 1999-09-07 | Agfa Gevaert Nv | ロール用フランジ |
| JP2009174991A (ja) * | 2008-01-24 | 2009-08-06 | Fujifilm Corp | 圧力測定シート |
| JP2009173307A (ja) * | 2008-01-24 | 2009-08-06 | Fujifilm Corp | 圧力測定シート |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2001331006A (ja) * | 2000-05-23 | 2001-11-30 | Fuji Photo Film Co Ltd | 感光材料ロールの支持体および包装体 |
| JP2002037528A (ja) * | 2000-07-19 | 2002-02-06 | Yano Shiki Kk | ロールペーパー保護具 |
| JP2002293481A (ja) * | 2001-03-29 | 2002-10-09 | Mitsubishi Paper Mills Ltd | 巻芯、写真用支持体用巻芯及びそれを用いた写真用支持体巻き取り |
-
2021
- 2021-01-26 CN CN202180013429.2A patent/CN117279850A/zh active Pending
- 2021-01-26 JP JP2022503173A patent/JP7360533B2/ja active Active
- 2021-01-26 WO PCT/JP2021/002553 patent/WO2021171868A1/ja not_active Ceased
- 2021-02-17 TW TW110105202A patent/TWI867157B/zh active
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH11240676A (ja) * | 1997-12-22 | 1999-09-07 | Agfa Gevaert Nv | ロール用フランジ |
| JP2009174991A (ja) * | 2008-01-24 | 2009-08-06 | Fujifilm Corp | 圧力測定シート |
| JP2009173307A (ja) * | 2008-01-24 | 2009-08-06 | Fujifilm Corp | 圧力測定シート |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7360533B2 (ja) | 2023-10-12 |
| JPWO2021171868A1 (cg-RX-API-DMAC7.html) | 2021-09-02 |
| TWI867157B (zh) | 2024-12-21 |
| TW202146322A (zh) | 2021-12-16 |
| CN117279850A (zh) | 2023-12-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN113330289B (zh) | 压力测定用材料及压力测定用材料的制造方法 | |
| CN113865767B (zh) | 压力测定用材料组合物、压力测定用材料及压力测定用材料组 | |
| JP7360533B2 (ja) | 組立体、圧力測定用シートセット | |
| JP7480187B2 (ja) | 組立体、圧力測定用シートセット、シート | |
| JP2009173307A (ja) | 圧力測定シート | |
| JP7398001B2 (ja) | 圧力測定用シートセット | |
| JP7100209B2 (ja) | 圧力測定用シートセット、圧力測定用シート、圧力測定用シートセットの製造方法、圧力測定用シートの製造方法 | |
| JP7231732B2 (ja) | 圧力測定用シートセット、圧力測定用シート | |
| JP7405999B2 (ja) | 圧力測定用シートセット | |
| JP7163514B2 (ja) | 圧力測定用シートセット及びその製造方法、圧力測定用シート及びその製造方法、分散液、並びに、マイクロカプセル | |
| WO2022137951A1 (ja) | 圧力測定用シートセット、圧力測定用シート、マイクロカプセル、分散液、圧力測定用シートセットの製造方法、圧力測定用シートの製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 21760818 Country of ref document: EP Kind code of ref document: A1 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202180013429.2 Country of ref document: CN |
|
| ENP | Entry into the national phase |
Ref document number: 2022503173 Country of ref document: JP Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 21760818 Country of ref document: EP Kind code of ref document: A1 |