EP3633076A1 - Molten salt titanium plating solution composition and method for manufacturing titanium-plated member - Google Patents
Molten salt titanium plating solution composition and method for manufacturing titanium-plated member Download PDFInfo
- Publication number
- EP3633076A1 EP3633076A1 EP18806263.2A EP18806263A EP3633076A1 EP 3633076 A1 EP3633076 A1 EP 3633076A1 EP 18806263 A EP18806263 A EP 18806263A EP 3633076 A1 EP3633076 A1 EP 3633076A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- plating solution
- solution composition
- molten
- titanium
- mol
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000007747 plating Methods 0.000 title claims abstract description 257
- 239000010936 titanium Substances 0.000 title claims abstract description 188
- 229910052719 titanium Inorganic materials 0.000 title claims abstract description 175
- 239000000203 mixture Substances 0.000 title claims abstract description 162
- RTAQQCXQSZGOHL-UHFFFAOYSA-N Titanium Chemical compound [Ti] RTAQQCXQSZGOHL-UHFFFAOYSA-N 0.000 title claims abstract description 161
- 238000004519 manufacturing process Methods 0.000 title claims description 39
- 238000000034 method Methods 0.000 title claims description 29
- 150000003839 salts Chemical class 0.000 title description 9
- 229910052751 metal Inorganic materials 0.000 claims abstract description 46
- 239000002184 metal Substances 0.000 claims abstract description 46
- -1 fluoride ions Chemical class 0.000 claims abstract description 38
- 150000002500 ions Chemical class 0.000 claims abstract description 25
- 229910001414 potassium ion Inorganic materials 0.000 claims abstract description 9
- WHXSMMKQMYFTQS-UHFFFAOYSA-N Lithium Chemical compound [Li] WHXSMMKQMYFTQS-UHFFFAOYSA-N 0.000 claims abstract description 7
- 229910052744 lithium Inorganic materials 0.000 claims abstract description 7
- 239000000758 substrate Substances 0.000 claims description 54
- 150000001768 cations Chemical class 0.000 claims description 15
- VEXZGXHMUGYJMC-UHFFFAOYSA-M Chloride anion Chemical compound [Cl-] VEXZGXHMUGYJMC-UHFFFAOYSA-M 0.000 claims description 10
- 239000012620 biological material Substances 0.000 claims description 9
- 150000001450 anions Chemical class 0.000 claims description 7
- 239000011734 sodium Substances 0.000 abstract description 8
- DGAQECJNVWCQMB-PUAWFVPOSA-M Ilexoside XXIX Chemical compound C[C@@H]1CC[C@@]2(CC[C@@]3(C(=CC[C@H]4[C@]3(CC[C@@H]5[C@@]4(CC[C@@H](C5(C)C)OS(=O)(=O)[O-])C)C)[C@@H]2[C@]1(C)O)C)C(=O)O[C@H]6[C@@H]([C@H]([C@@H]([C@H](O6)CO)O)O)O.[Na+] DGAQECJNVWCQMB-PUAWFVPOSA-M 0.000 abstract description 7
- 229910052708 sodium Inorganic materials 0.000 abstract description 7
- 239000000243 solution Substances 0.000 description 140
- 238000002474 experimental method Methods 0.000 description 35
- PXHVJJICTQNCMI-UHFFFAOYSA-N nickel Substances [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 description 25
- 239000000047 product Substances 0.000 description 22
- ATJFFYVFTNAWJD-UHFFFAOYSA-N Tin Chemical compound [Sn] ATJFFYVFTNAWJD-UHFFFAOYSA-N 0.000 description 19
- KWGKDLIKAYFUFQ-UHFFFAOYSA-M lithium chloride Chemical compound [Li+].[Cl-] KWGKDLIKAYFUFQ-UHFFFAOYSA-M 0.000 description 19
- 230000000052 comparative effect Effects 0.000 description 18
- ZLMJMSJWJFRBEC-UHFFFAOYSA-N Potassium Chemical compound [K] ZLMJMSJWJFRBEC-UHFFFAOYSA-N 0.000 description 16
- 230000007797 corrosion Effects 0.000 description 15
- 238000005260 corrosion Methods 0.000 description 15
- PQXKHYXIUOZZFA-UHFFFAOYSA-M lithium fluoride Chemical compound [Li+].[F-] PQXKHYXIUOZZFA-UHFFFAOYSA-M 0.000 description 15
- FAPWRFPIFSIZLT-UHFFFAOYSA-M Sodium chloride Chemical compound [Na+].[Cl-] FAPWRFPIFSIZLT-UHFFFAOYSA-M 0.000 description 13
- PUZPDOWCWNUUKD-UHFFFAOYSA-M sodium fluoride Chemical compound [F-].[Na+] PUZPDOWCWNUUKD-UHFFFAOYSA-M 0.000 description 13
- XJDNKRIXUMDJCW-UHFFFAOYSA-J titanium tetrachloride Chemical compound Cl[Ti](Cl)(Cl)Cl XJDNKRIXUMDJCW-UHFFFAOYSA-J 0.000 description 13
- 229910052700 potassium Inorganic materials 0.000 description 12
- 239000011591 potassium Substances 0.000 description 12
- 229910020491 K2TiF6 Inorganic materials 0.000 description 11
- 239000011698 potassium fluoride Substances 0.000 description 11
- 239000000446 fuel Substances 0.000 description 9
- XEEYBQQBJWHFJM-UHFFFAOYSA-N iron Substances [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 9
- 229910052759 nickel Inorganic materials 0.000 description 9
- 229910003074 TiCl4 Inorganic materials 0.000 description 8
- 239000003795 chemical substances by application Substances 0.000 description 8
- 230000008018 melting Effects 0.000 description 8
- 238000002844 melting Methods 0.000 description 8
- 239000002504 physiological saline solution Substances 0.000 description 8
- 239000011148 porous material Substances 0.000 description 8
- 229910001416 lithium ion Inorganic materials 0.000 description 7
- 150000003609 titanium compounds Chemical class 0.000 description 7
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 7
- 230000002159 abnormal effect Effects 0.000 description 6
- 239000003792 electrolyte Substances 0.000 description 6
- 239000005518 polymer electrolyte Substances 0.000 description 6
- 235000013024 sodium fluoride Nutrition 0.000 description 6
- 239000011775 sodium fluoride Substances 0.000 description 6
- 229910001415 sodium ion Inorganic materials 0.000 description 6
- 238000005868 electrolysis reaction Methods 0.000 description 5
- 238000011156 evaluation Methods 0.000 description 5
- 229910052742 iron Inorganic materials 0.000 description 5
- NROKBHXJSPEDAR-UHFFFAOYSA-M potassium fluoride Chemical compound [F-].[K+] NROKBHXJSPEDAR-UHFFFAOYSA-M 0.000 description 5
- 239000013535 sea water Substances 0.000 description 5
- 239000011780 sodium chloride Substances 0.000 description 5
- 239000012459 cleaning agent Substances 0.000 description 4
- 238000002484 cyclic voltammetry Methods 0.000 description 4
- 230000003746 surface roughness Effects 0.000 description 4
- 239000000956 alloy Substances 0.000 description 3
- 229910045601 alloy Inorganic materials 0.000 description 3
- 239000007864 aqueous solution Substances 0.000 description 3
- 239000007789 gas Substances 0.000 description 3
- 239000001257 hydrogen Substances 0.000 description 3
- 229910052739 hydrogen Inorganic materials 0.000 description 3
- 238000009616 inductively coupled plasma Methods 0.000 description 3
- 239000000463 material Substances 0.000 description 3
- 239000000843 powder Substances 0.000 description 3
- KRHYYFGTRYWZRS-UHFFFAOYSA-N Fluorane Chemical compound F KRHYYFGTRYWZRS-UHFFFAOYSA-N 0.000 description 2
- KRHYYFGTRYWZRS-UHFFFAOYSA-M Fluoride anion Chemical compound [F-] KRHYYFGTRYWZRS-UHFFFAOYSA-M 0.000 description 2
- UFHFLCQGNIYNRP-UHFFFAOYSA-N Hydrogen Chemical compound [H][H] UFHFLCQGNIYNRP-UHFFFAOYSA-N 0.000 description 2
- 229910020312 KCl—KF Inorganic materials 0.000 description 2
- GRYLNZFGIOXLOG-UHFFFAOYSA-N Nitric acid Chemical compound O[N+]([O-])=O GRYLNZFGIOXLOG-UHFFFAOYSA-N 0.000 description 2
- GWEVSGVZZGPLCZ-UHFFFAOYSA-N Titan oxide Chemical compound O=[Ti]=O GWEVSGVZZGPLCZ-UHFFFAOYSA-N 0.000 description 2
- 238000004140 cleaning Methods 0.000 description 2
- 239000013065 commercial product Substances 0.000 description 2
- NMGYKLMMQCTUGI-UHFFFAOYSA-J diazanium;titanium(4+);hexafluoride Chemical compound [NH4+].[NH4+].[F-].[F-].[F-].[F-].[F-].[F-].[Ti+4] NMGYKLMMQCTUGI-UHFFFAOYSA-J 0.000 description 2
- RXCBCUJUGULOGC-UHFFFAOYSA-H dipotassium;tetrafluorotitanium;difluoride Chemical compound [F-].[F-].[F-].[F-].[F-].[F-].[K+].[K+].[Ti+4] RXCBCUJUGULOGC-UHFFFAOYSA-H 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- XLYOFNOQVPJJNP-ZSJDYOACSA-N heavy water Substances [2H]O[2H] XLYOFNOQVPJJNP-ZSJDYOACSA-N 0.000 description 2
- 229910001512 metal fluoride Inorganic materials 0.000 description 2
- 229910017604 nitric acid Inorganic materials 0.000 description 2
- NRNCYVBFPDDJNE-UHFFFAOYSA-N pemoline Chemical compound O1C(N)=NC(=O)C1C1=CC=CC=C1 NRNCYVBFPDDJNE-UHFFFAOYSA-N 0.000 description 2
- 235000003270 potassium fluoride Nutrition 0.000 description 2
- MYYUWUVATCWCES-UHFFFAOYSA-L potassium;oxalate;titanium(4+);dihydrate Chemical compound O.O.[K+].[Ti+4].[O-]C(=O)C([O-])=O MYYUWUVATCWCES-UHFFFAOYSA-L 0.000 description 2
- 238000002360 preparation method Methods 0.000 description 2
- 239000000779 smoke Substances 0.000 description 2
- VWDWKYIASSYTQR-UHFFFAOYSA-N sodium nitrate Chemical compound [Na+].[O-][N+]([O-])=O VWDWKYIASSYTQR-UHFFFAOYSA-N 0.000 description 2
- 239000000126 substance Substances 0.000 description 2
- 238000012360 testing method Methods 0.000 description 2
- OGIDPMRJRNCKJF-UHFFFAOYSA-N titanium oxide Inorganic materials [Ti]=O OGIDPMRJRNCKJF-UHFFFAOYSA-N 0.000 description 2
- 229910019985 (NH4)2TiF6 Inorganic materials 0.000 description 1
- 229910003708 H2TiF6 Inorganic materials 0.000 description 1
- 229910011530 LiF—NaCl Inorganic materials 0.000 description 1
- 229910011526 LiF—NaF Inorganic materials 0.000 description 1
- HBBGRARXTFLTSG-UHFFFAOYSA-N Lithium ion Chemical compound [Li+] HBBGRARXTFLTSG-UHFFFAOYSA-N 0.000 description 1
- 229910021607 Silver chloride Inorganic materials 0.000 description 1
- 229910010062 TiCl3 Inorganic materials 0.000 description 1
- 238000004458 analytical method Methods 0.000 description 1
- QVGXLLKOCUKJST-UHFFFAOYSA-N atomic oxygen Chemical compound [O] QVGXLLKOCUKJST-UHFFFAOYSA-N 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 230000006866 deterioration Effects 0.000 description 1
- 238000002845 discoloration Methods 0.000 description 1
- 230000005496 eutectics Effects 0.000 description 1
- 210000003709 heart valve Anatomy 0.000 description 1
- 150000002431 hydrogen Chemical class 0.000 description 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-M hydroxide Chemical compound [OH-] XLYOFNOQVPJJNP-UHFFFAOYSA-M 0.000 description 1
- 238000004255 ion exchange chromatography Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- YOYLLRBMGQRFTN-SMCOLXIQSA-N norbuprenorphine Chemical compound C([C@@H](NCC1)[C@]23CC[C@]4([C@H](C3)C(C)(O)C(C)(C)C)OC)C3=CC=C(O)C5=C3[C@@]21[C@H]4O5 YOYLLRBMGQRFTN-SMCOLXIQSA-N 0.000 description 1
- 239000001301 oxygen Substances 0.000 description 1
- 229910052760 oxygen Inorganic materials 0.000 description 1
- 239000002244 precipitate Substances 0.000 description 1
- 230000001681 protective effect Effects 0.000 description 1
- 238000001878 scanning electron micrograph Methods 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- HKZLPVFGJNLROG-UHFFFAOYSA-M silver monochloride Chemical compound [Cl-].[Ag+] HKZLPVFGJNLROG-UHFFFAOYSA-M 0.000 description 1
- 235000010344 sodium nitrate Nutrition 0.000 description 1
- 239000004317 sodium nitrate Substances 0.000 description 1
- 238000004611 spectroscopical analysis Methods 0.000 description 1
- YONPGGFAJWQGJC-UHFFFAOYSA-K titanium(iii) chloride Chemical compound Cl[Ti](Cl)Cl YONPGGFAJWQGJC-UHFFFAOYSA-K 0.000 description 1
- 210000004746 tooth root Anatomy 0.000 description 1
- 238000011179 visual inspection Methods 0.000 description 1
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D3/00—Electroplating: Baths therefor
- C25D3/66—Electroplating: Baths therefor from melts
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D5/00—Electroplating characterised by the process; Pretreatment or after-treatment of workpieces
- C25D5/34—Pretreatment of metallic surfaces to be electroplated
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D7/00—Electroplating characterised by the article coated
Definitions
- the present disclosure relates to a molten-salt titanium plating solution composition and a method for manufacturing a titanium-plated member.
- the present disclosure claims priority to Japanese Patent Application No. 2017-100757 filed on May 22, 2017 , the disclosure of which is hereby incorporated by reference in its entirety.
- Patent Laying-Open No. 2015-193899 discloses that a plating bath containing KF-KCl to which K 2 TiF 6 and TiO 2 are added is used to form an alloy film of Fe and Ti on the surface of an Fe wire.
- NPL 1 discloses that a plating bath containing LiF-NaF-KF to which K 2 TiF 6 is added is used to form a titanium film on the surface of a substrate of Ni and Fe.
- NPL 1 A. ROBIN et.al., "ELECTOLYTIC COATING OF TITANIUM ONTO IRON AND NICKEL ELECTRODES IN THE MOLTEN LiF+NaF+KF EUTECTIC", Journal of Electroanal. Chem., 230 (1987), pp. 125-141
- a molten-salt titanium plating solution composition contains: ions of at least one Group I metal selected from the group of lithium and sodium, fluoride ions, and titanium ions.
- the molten-salt titanium plating solution composition contains less than or equal to 5 mol% of potassium ions with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition.
- a method for manufacturing a titanium-plated member includes: preparing a substrate having an electrically conductive surface; immersing the substrate in the molten-salt titanium plating solution composition; and forming a titanium plating film on the surface of the substrate by applying electric current to cause the substrate immersed in the molten-salt titanium plating solution composition to serve as a cathode and cause the surface of the substrate to be coated with titanium.
- fluoride ions F -
- fluoride ions F -
- fluoride ions F -
- fluoride ion source potassium fluoride (KF) is widely used.
- KF is a good fluoride ion source, and a molten-salt titanium plating solution composition containing potassium ions (K + ) generated from KF exhibits good plating performance in titanium plating.
- the molten-salt titanium plating solution composition enables generation of metal fog during plating to be suppressed.
- a to B herein specifies an upper limit and a lower limit of a range (i.e., more than or equal to A and less than or equal to B).
- A is not accompanied by a unit but only B is accompanied by a unit
- the unit for B is identical to the unit for A.
- a molten-salt titanium plating solution composition in the present embodiment contains ions of at least one Group I metal selected from the group of lithium (Li + ) and sodium (Na + ), fluoride ions (F - ), and titanium ions (Ti n+ (n is an integer of 2 or more and 4 or less, the same applies as well to the following)).
- the plating solution composition contains less than or equal to 5 mol% of potassium ions (K + ) with respect to 100 mol% of all ion components contained in the plating solution composition.
- the plating solution composition further contains chloride ions (Cl - ).
- the plating solution composition can be prepared as a molten salt by dissolving a titanium compound serving as a source of Ti n+ in a mixture of at least one of lithium fluoride (LiF) and sodium fluoride (NaF) and at least one of lithium chloride (LiCl) and sodium chloride (NaCl), for example.
- the plating solution composition may contain, as Ti n+ in a titanium compound, multiple types of titanium that are different in valence.
- Examples of the titanium compound serving as a source of Ti n+ may include hexafluorotitanic acid (H 2 TiF 6 ), potassium hexafluorotitanate (K 2 TiF 6 ), ammonium hexafluorotitanate ((NH 4 ) 2 TiF 6 ), sodium hexafluorotitanate (Na 2 TiF 6 ), potassium titanium oxalate dihydrate (K 2 TiO(C 2 O 4 ) 2 • 2H 2 O), titanium chloride (III)(TiCl 3 ), titanium chloride (IV)(TiCl 4 ), and the like.
- H 2 TiF 6 hexafluorotitanic acid
- K 2 TiF 6 potassium hexafluorotitanate
- ammonium hexafluorotitanate (NH 4 ) 2 TiF 6 )
- sodium hexafluorotitanate Na 2 TiF 6
- potassium titanium oxalate dihydrate K 2 Ti
- Potassium hexafluorotitanate (K 2 TiF 6 ) and potassium titanium oxalate dihydrate (K 2 TiO(C 2 O 4 ) 2 • 2H 2 O) contain potassium ions, and therefore, these titanium compounds are used at respective contents so that the K + content with respect to 100 mol% of all ion components contained in the plating solution composition is less than or equal to 5 mol%, or these titanium compounds are used together with another titanium compound (such as titanium chloride (IV) or the like, for example) that generates no K + .
- another titanium compound such as titanium chloride (IV) or the like, for example
- LiF, NaF, LiCl, and NaCl are ionized to be present in the form of Li + , Na + , F - , and Cl - .
- the titanium compound is also ionized to be present in the form of Ti n+ . It is preferable to prepare, as a molten salt, a plating solution composition containing: ions of at least one Group I metal selected from the group of Li + and Na + ; F - ; Cl - ; and Ti n+ in this way.
- Li + , Na + , F - , Cl - , and Ti n+ are present in the plating solution composition of the present embodiment can be confirmed, for example, by dissolving the plating solution composition in a solution of a mixture of nitric acid and hydrofluoric acid, and analyzing the solution by ICP (Inductively Coupled Plasma Spectrometry) or IC analysis (Ion Chromatography).
- ICP Inductively Coupled Plasma Spectrometry
- IC analysis Ion Chromatography
- ICP apparatus iCAP6200 or the like manufactured by Thermo Fisher Scientific Inc. may be used, for example.
- the ratio of the fluoride ions to all anions contained in the molten-salt titanium plating solution composition may be more than or equal to 30 mol% and less than or equal to 100 mol%.
- the molten-salt titanium plating solution composition containing fluoride ions at such a ratio enables manufacture of a titanium-plated member having a titanium plating film excellent in surface smoothness.
- the ratio of fluoride ions to all anions is preferably more than or equal to 40 mol% and less than or equal to 90 mol%, and more preferably more than or equal to 45 mol% and less than or equal to 75 mol%.
- the content of F - with respect to 100 mol% of a total of Cl - and F - is more than or equal to 30 mol% and less than or equal to 50 mol%.
- the melting point of the plating solution composition is once reduced by depression of melting point, and thereafter increased again.
- the melting point depression effect is large when the ratio of the F - content relative to 100 mol% of the total content of Cl - and F - falls in a predetermined range.
- reduction of the melting point is large when the content of F - with respect to 100 mol% of the total of Cl - and F - is more than or equal to 30 mol% and less than or equal to 50 mol%, which facilitates plating at a lower temperature. More preferably, the content of F - with respect to 100 mol% of the total of Cl - and F - is more than or equal to 30 mol% and less than or equal to 45 mol%, because reduction of the melting point is larger.
- the content of Ti n+ in the plating solution composition is not particularly limited, but set appropriately depending on plating conditions. However, an excessively high content of Ti n+ may cause unnecessary precipitates to be formed, which increases reduction of current efficiency. In contrast, an excessively low content of Ti n+ does not allow a titanium plating film to be formed sufficiently.
- the content of Ti n+ is therefore preferably less than or equal to 20 mol% and more preferably less than or equal to 12 mol%, with respect to 100 mol% of all cations in the plating solution composition.
- the content of Ti n+ is preferably more than or equal to 0.1 mol%, and more preferably more than or equal to 0.5 mol%, with respect to 100 mol% of all cations in the plating solution composition. In other words, the content of titanium ions with respect to 100 mol% of all cations contained in the molten-salt titanium plating solution composition is preferably more than or equal to 0.1 mol% and less than or equal to 12 mol%.
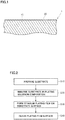
- Fig. 1 is a schematic cross-sectional view showing an example of a part of a titanium-plated member.
- Fig. 2 is a flowchart showing a procedure for manufacturing a titanium-plated member.
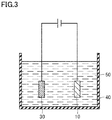
- Fig. 3 is a schematic cross-sectional view showing an example of a state in which a substrate is immersed in a molten-salt titanium plating solution composition.
- a titanium-plated member 1 is made up of a substrate 10 and a titanium plating film 20 (hereinafter also referred to simply as "plating film 20") formed on a surface of substrate 10.
- Plating film 20 is a film made of titanium.
- titanium-plated member 1 is manufactured through steps S10 to S40 shown in Fig. 2 .
- a method for manufacturing titanium-plated member 1 includes: the step of preparing substrate 10 having an electrically conductive surface (S10); the step of immersing substrate 10 in plating solution composition 50 (S20); and the step of forming titanium plating film 20 on the surface of substrate 10 by applying electric current to cause substrate 10 immersed in plating solution composition 50 to serve as a cathode and cause the surface of substrate 10 to be coated with titanium (S30). Further, the method for manufacturing titanium-plated member 1 preferably includes the step of cleaning a surface of plating film 20 (S40). The method for manufacturing titanium-plated member 1 of the present embodiment may include any step besides the steps S10, S20, S30, and S40. In the following, each of these steps is described.
- substrate 10 having an electrically conductive surface is prepared (S10).
- the material forming substrate 10 is not particularly limited as long as the material has an electrically conductive surface.
- Examples of substrate 10 include, for example, a substrate made of iron or nickel, a substrate made of an alloy of them, or a multilayer substrate having a surface made of a layer of iron or nickel or an alloy thereof.
- substrate 10 is not particularly limited.
- substrate 10 in the shape of any of various shapes such as plate, column, pipe, mesh, or the like may be employed as substrate 10.
- plating solution composition 50 As plating solution composition 50, a plating solution composition prepared in the above-described way is used.
- plating solution composition 50 contains ions of at least one Group I metal selected from the group of lithium (Li + ) and sodium (Na + ), fluoride ions (F - ), titanium ions (Ti n+ ), and chloride ions (Cl - ). Further, plating solution composition 50 is prepared so that the content of potassium ions (K + ) with respect to 100 mol% of all ion components contained in plating solution composition 50 is less than or equal to 5 mol%.
- Group I metal selected from the group of lithium (Li + ) and sodium (Na + ), fluoride ions (F - ), titanium ions (Ti n+ ), and chloride ions (Cl - ).
- plating solution composition 50 is prepared so that the content of potassium ions (K + ) with respect to 100 mol% of all ion components contained in plating solution composition 50 is less than or equal to 5 mol%.
- plating solution composition 50 is prepared so that the ratio of the fluoride ions to all anions contained in the molten-salt titanium plating solution composition is more than or equal to 30 mol% and less than or equal to 100 mol%. Further, preferably plating solution composition 50 is prepared so that plating solution composition 50 contains more than or equal to 30 mol% and less than or equal to 50 mol% of F - , with respect to 100 mol% of the total of Cl - and F - . Preferably plating solution composition 50 is prepared so that plating solution composition 50 contains more than or equal to 0.1 mol% and less than or equal to 12 mol% of Ti n+ with respect to 100 mol% of all cations contained in plating solution composition 50.
- plating film 20 is formed on the surface of substrate 10.
- Electrolysis of plating solution composition 50 is preferably performed so that the absolute value of the current density, on substrate 10, of current flowing between anode 30 and substrate 10 is more than or equal to 1 mA/cm 2 and less than or equal to 500 mA/cm 2 , and more preferably performed so that the absolute value of the current density is more than or equal to 1 mA/cm 2 and less than or equal to 300 mA/cm 2 .
- plating film 20 can be formed on the surface of substrate 10 in a shorter time.
- plating film 20 having higher surface smoothness can be formed.
- a cleaning agent can be used to clean the surface of plating film 20 to thereby remove the components remaining on the surface of plating film 20.
- water may be used.
- substrate 10 on which plating film 20 is formed may be cleaned with water.
- a cleaning agent other than water may be used such as a cleaning agent containing water-soluble salt having a high compatibility with components contained in plating solution composition 50, instead of or in combination with water. In this way, titanium-plated member 1 having a surface of substrate 10 coated with plating film 20 is manufactured.
- Titanium-plated member 1 manufactured in this way can be used in a variety of fields, as a member having a protective film with a high hardness and a high surface smoothness as well as excellent corrosion resistance and excellent wear resistance.
- the ratio of average surface roughness Ra to average thickness R of plating film 20 ((Ra/R) ⁇ 100 (%)) of titanium-plated member 1 manufactured by the above-described method is preferably less than or equal to 10%, and more preferably less than or equal to 5%. With the ratio falling in this range, titanium-plated member 1 having plating film 20 with a sufficiently high surface smoothness can be provided.
- Average surface roughness Ra of plating film 20 can be measured through observation of a cross section with an SEM (Scanning Electron Microscope) or by means of a surface roughness meter. Average thickness R of plating film 20 can be determined through observation of a cross section with an SEM. Average surface roughness Ra of plating film 20 refers to an arithmetic mean roughness Ra specified under JIS B 0601 (2001). Average thickness R of plating film 20 may be an arithmetic mean thickness of plating film 20 determined from thicknesses at any 10 points on an SEM image, for example.
- SEM Scnning Electron Microscope
- the molten-salt titanium plating solution composition is used for manufacturing an insoluble electrode.
- a molten-salt titanium plating solution composition for manufacturing an insoluble electrode an insoluble electrode having a titanium plating film excellent in surface smoothness can be manufactured.
- the insoluble electrode is used for manufacturing hydrogen.
- the electrode can be provided as a hydrogen-manufacturing insoluble electrode with a low resistance. Accordingly, hydrogen with a high purity can be manufactured.
- the molten-salt titanium plating solution composition is used for manufacturing a current collector.
- a current collector having a titanium plating film with excellent surface smoothness can be manufactured.
- the current collector is used for a fuel cell.
- a current collector for a fuel cell can be provided as a fuel-cell current collector having a good electrical conductivity.
- the current collector is more preferably used for a polymer electrolyte fuel cell.
- the molten-salt titanium plating solution composition is used for manufacturing a biomaterial.
- a biomaterial-manufacturing molten-salt titanium plating solution composition a biomaterial having a titanium plating film with an excellent surface smoothness can be manufactured. This biomaterial is also excellent in corrosion resistance.
- the use of the biomaterial is preferably selected from the group consisting of spinal fixation device, fracture fixation device, artificial joint, artificial heart valve, intravascular stent, denture base, artificial dental root, and orthodontic wire.
- molten-salt titanium plating solution composition 50 according to the present embodiment enables generation of metal fog during plating to be suppressed. Further, in accordance with the method for manufacturing titanium-plated member 1, titanium-plated member 1 having plating film 20 with high surface smoothness can be manufactured.
- molten-salt titanium plating solution composition 50 containing chloride ions (Cl - ) is described. Molten-salt titanium plating solution composition 50, however, may be prepared without containing Cl - . As a molten-salt titanium plating solution composition 50 containing no Cl - , molten-salt titanium plating solution composition 50 can be prepared to contain other anions instead of Cl - . In this case, the aforementioned other anions are preferably selected that are stable at the plating temperature and will not form a residue such as salt that is difficult to remove after plating.
- plating solution composition 50 is prepared to contain more than or equal to 30 mol% and less than or equal to 50 mol% of F - with respect to 100 mol% of the total of Cl - and F - , and contain more than or equal to 0.1 mol% and less than or equal to 12 mol% of Ti n+ with respect to 100 mol% of all cations contained in plating solution composition 50.
- the limitations on respective contents are not requisite ones. The contents can be set appropriately in consideration of the required plating temperature and plating performance.
- Experiment No. 1 is an example where a plating solution composition of an Example within the range of the molten-salt titanium plating solution composition of the present disclosure was used.
- Experiment Nos. 2 to 4 are each an example where a plating solution composition of a comparative example out of the range of the molten-salt titanium plating solution composition of the present disclosure was used.
- Molten-salt titanium plating solution compositions of Experiment Nos. 1 to 4 were each prepared by dissolving, in the main agent for the plating solution composition shown in Table 1, one or both of K 2 TiF 6 powder and TiCl 4 gas as a titanium source at a ratio of 2 mol of the total of one or both of K 2 TiF 6 powder and TiCl 4 gas with respect to 100 mol of the main agent. Further, through the steps S10 to S40 of the method for manufacturing a titanium-plated member as described above (see Fig. 2 ), each of the molten-salt titanium plating solution compositions of Experiment Nos.
- the ratio of an abnormal plating portion resulting from discoloration of the plated surface and/or lack of plating on the surface to be plated was evaluated based on the area ratio (%) of the abnormal plating portion.
- the level of the plating performance is classified into those termed "good,” “average,” “somewhat poor” and “poor” respectively. “Good” means that the abnormal portion is less than 5%, “average” means that the abnormal portion is more than or equal to 5% and less than 20 %, “somewhat poor” means that the abnormal portion is more than or equal to 20% and less than 50%, and “poor” means that the abnormal portion is more than or equal to 50%.
- the plating performance was good and generation of metal fog was not confirmed.
- generation of metal fog of potassium could be suppressed by performing titanium plating using a molten-salt titanium plating solution composition in which the content of K + with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition was less than or equal to 5 mol%.
- the plating performance was also good in the case of a molten-salt titanium plating solution composition containing K + at a smaller content and containing Li + as main cations instead.
- Molten-salt titanium plating solution compositions of Experiment Nos. 5 to 16 were each prepared by dissolving, in the main agent for the plating solution composition shown in Tables 2 to 4, one or both of K 2 TiF 6 powder and TiCl 4 gas as a titanium source at the ratio shown in Tables 2 to 4 with respect to 100 mol of the main agent.
- the molten-salt titanium plating solution composition of Experiment No. 5 contains more than 5 mol% of K + with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition, and is therefore a Comparative Example.
- Respective molten-salt titanium plating solution compositions of Experiment Nos. 6 to 16 each contain less than or equal to 5 mol% of K + with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition, and are therefore Examples.
- Respective molten-salt titanium plating solution compositions of Experiment Nos. 7 and 15 are Examples containing no chloride ions.
- Respective molten-salt titanium plating solution compositions of Experiment No. 8, Nos. 10 to 12, and No. 16 are Examples in which the content of fluoride ions with respect to 100 mol% of the total of chloride ions and fluoride ions is more than or equal to 30 mol% and less than or equal to 50 mol%.
- the molten-salt titanium plating solution composition of Experiment No. 12 contains more than 12 mol% of titanium ions with respect to 100 mol% of all cations contained in the molten-salt titanium plating solution composition.
- the molten-salt titanium plating solution composition of Experiment No. 16 contains less than 0.1 mol% of titanium ions with respect to 100 mol% of all cations contained in the molten-salt titanium plating solution composition.
- each of the molten-salt titanium plating solution compositions of Experiment Nos. 5 to 16 was used to plate a surface of a respective substrate (made of nickel, 0.1 mm in thickness, 5 mm ⁇ 25 mm in size) with titanium through the steps S10 to S40 of the method for manufacturing a titanium-plated member as described above (see Fig. 2 ).
- titanium-plated members of Experiment Nos. 5 to 16 were manufactured.
- the plating performance was evaluated by the same evaluation method as Example 1.
- whether or not metal fog was generated in the process of titanium plating was also confirmed by the same evaluation method as Example 1. The results are shown in Tables 2 to 4.
- LiF-KCl-KF LiF-KCl-KF LiF LiF-LiCl makeup of plating solution composition (molar ratio) LiF 45 45 100 30 LiCl 55 55 0 70 NaF 0 0 0 0 KF 8 6 0 0 KCl 0 0 0 K 2 TiF 6 2 2 2 2 TiCl 4 0 0 0 0 ratio of K + (mol%) to 100 mol% of all ion components 5.1 4.3 1.8 1.8 F - /(Cl - +F - ) (mol%) 54 53 100 38 ratio of Ti n+ (mol%) to 100 mol% of all cations 1.8 1.8 1.9 1.9 plating temperature (°C) 650 650 900 650 plating performance good good good good good generation of metal fog small amount was generated not generated not generated not generated not generated [Table 3] Experiment No.
- molten-salt titanium plating solution composition 50 and the method for manufacturing titanium-plated member 1 according to the present embodiment enable generation of metal fog during plating to be suppressed.
- the molten-salt titanium plating solution composition of Experiment No. 8 was used and, through the steps S10 to S40 of the method for manufacturing a titanium-plated member described above (see Fig. 2 ), the surface of a nickel porous substrate (3 cm ⁇ 5 cm ⁇ 1 mmt, porosity: 96%, average pore size: 300 ⁇ m, hereinafter referred to as "nickel porous material") was plated with titanium.
- nickel porous material 3 cm ⁇ 5 cm ⁇ 1 mmt, porosity: 96%, average pore size: 300 ⁇ m, hereinafter referred to as "nickel porous material"
- a Ni porous material product name: "Celmet®” manufactured by Sumitomo Electric Industries, Ltd.
- a Ti metal sheet manufactured by Nilaco Corporation
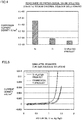
- the Ti-plated product of the Example is lower in corrosion current density than the Ni porous material of the Comparative Example, and is thus stable in an environment of physiological saline solution. It is seen from this result that the Ti-plated product of the Example is suitable as a biomaterial. Further, the Ti-plated product of the Example is lower in corrosion current density than the Ti metal sheet of the Comparative Example. It is seen from this result that the structure of a metal porous material instead of a metal sheet is used to further improve the stability in an environment of physiological saline solution.
- the corrosion resistance of the following Ti-plated product to saline solution simulating seawater was evaluated through the following procedure.
- Example 3 As a specimen of the Example, a Ti-plated product manufactured by the same method as the Ti-plated product used for Example 3 was prepared. As a specimen of the Comparative Example, a Ti metal sheet (manufactured by Nilaco Corporation) was prepared.
- the Ti-plated product of the Example is lower in current density than the Ti commercial product of the Comparative Example, and thus exhibits high corrosion resistance to seawater. It is seen from the above that the Ti-plated product of the Example is promising as an insoluble electrode (anode) for electrolysis of salt.
- Example 3 As a specimen of the Example, a Ti-plated product manufactured by the same method as the Ti-plated product used in Example 3 was prepared. As specimens of the Comparative Example, an Ni porous material (product name: "Celmet®” manufactured by Sumitomo Electric Industries, Ltd.) and a Ti metal sheet (manufactured by Nilaco Corporation) were prepared.
- Ni porous material product name: "Celmet®” manufactured by Sumitomo Electric Industries, Ltd.
- Ti metal sheet manufactured by Nilaco Corporation
- Fig. 7 shows these plots by expanding the scale of the vertical axis (current density) so that the plot depicting the correlation for "Ti-plated product” can be distinguished from the plot depicting the correlation for "comparative Ti.”
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Electroplating Methods And Accessories (AREA)
Abstract
Description
- The present disclosure relates to a molten-salt titanium plating solution composition and a method for manufacturing a titanium-plated member. The present disclosure claims priority to Japanese Patent Application No.
2017-100757 filed on May 22, 2017 - As a titanium plating method, a method of plating in molten salt has been studied. For example, Japanese Patent Laying-Open No.
2015-193899 - PTL 1: Japanese Patent Laying-Open No.
2015-193899 - NPL 1: A. ROBIN et.al., "ELECTOLYTIC COATING OF TITANIUM ONTO IRON AND NICKEL ELECTRODES IN THE MOLTEN LiF+NaF+KF EUTECTIC", Journal of Electroanal. Chem., 230 (1987), pp. 125-141
- According to an aspect of the present disclosure, a molten-salt titanium plating solution composition contains: ions of at least one Group I metal selected from the group of lithium and sodium, fluoride ions, and titanium ions. The molten-salt titanium plating solution composition contains less than or equal to 5 mol% of potassium ions with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition.
- According to an aspect of the present disclosure, a method for manufacturing a titanium-plated member includes: preparing a substrate having an electrically conductive surface; immersing the substrate in the molten-salt titanium plating solution composition; and forming a titanium plating film on the surface of the substrate by applying electric current to cause the substrate immersed in the molten-salt titanium plating solution composition to serve as a cathode and cause the surface of the substrate to be coated with titanium.
-
-
Fig. 1 is a schematic cross-sectional view showing an example of a part of a titanium-plated member. -
Fig. 2 is a flowchart showing a procedure for manufacturing a titanium-plated member. -
Fig. 3 is a schematic cross-sectional view showing an example of a state in which a substrate is immersed in a molten-salt titanium plating solution composition. -
Fig. 4 is a graph showing the corrosion current density of each electrode in a physiological saline solution. -
Fig. 5 is a graph showing a correlation between the potential and the current density of each electrode in a simulated seawater. -
Fig. 6 is a graph showing a correlation between the potential and the current density of each electrode in a simulated electrolyte for a polymer electrolyte fuel cell (PEFC). -
Fig. 7 is another graph showing a correlation between the potential and the current density of each electrode in a simulated electrolyte for a polymer electrolyte fuel cell (PEFC). - In order to obtain a film having a smooth surface in titanium plating, it is important that fluoride ions (F-) be present in a molten-salt titanium plating solution composition. As a fluoride ion source, potassium fluoride (KF) is widely used. KF is a good fluoride ion source, and a molten-salt titanium plating solution composition containing potassium ions (K+) generated from KF exhibits good plating performance in titanium plating.
- According to studies by the inventors, it has been found that titanium plating performed in a plating bath containing a high content of K+ results in metal fog of potassium and generation of potassium metal in the plating bath. Further, it has also been found that the current efficiency is deteriorated due to current flowing through the potassium metal between a cathode and an anode during plating.
- It is one of objects to provide a molten-salt titanium plating solution composition that enables generation of metal fog during plating to be suppressed.
- The molten-salt titanium plating solution composition enables generation of metal fog during plating to be suppressed.
- Initially, embodiments of the present disclosure are described one by one.
- [1] According to an aspect of the present disclosure, a molten-salt titanium plating solution composition (hereinafter also referred to as "plating solution composition") contains: ions of at least one Group I metal selected from the group of lithium and sodium, fluoride ions, and titanium ions. The molten-salt titanium plating solution composition contains less than or equal to 5 mol% of potassium ions with respect to 100 mol% of all ion components contained in the plating solution composition.
Because of a strong bonding strength of titanium with oxygen, titanium is likely to react with water to form oxide and hydroxide, and is therefore not suitable for plating from an aqueous solution. In order to form a titanium plating film on a substrate, a plating bath of a molten-salt titanium plating solution composition made up of a molten salt containing titanium ions is therefore used.
It is known that, in order to obtain a titanium plating film having a smooth surface from a molten-salt titanium plating solution composition, the presence of fluoride ions in the molten-salt titanium plating solution composition is important. Therefore, as a molten-salt titanium plating solution composition, a composition containing a predetermined amount of a metal fluoride serving as a source of fluoride ions is selected. Potassium fluoride is used as a metal fluoride serving as a source of fluoride ions.
According to studies by the inventors, however, when a titanium plating film is formed from a plating solution containing a high content of potassium fluoride, metal fog of potassium is generated during formation of the plating film. Because there is a sufficient separation between the redox potential of potassium and the redox potential of titanium, usually potassium is not electrodeposited in a condition where titanium is electrodeposited. Metal fog of potassium, however, has a redox potential closer to the redox potential of titanium. Therefore, in a condition where titanium is electrodeposited, metal fog of potassium is likely to be generated simultaneously.
If metal fog is generated, potassium metal suspends in the plating bath. During plating, current flows through the potassium metal between a cathode and an anode, resulting in deterioration of current efficiency. It is therefore necessary to suppress generation of metal fog from the plating bath.
The molten-salt titanium plating solution composition of the present disclosure can form a titanium plating film having high surface smoothness while suppressing generation of metal fog. Specifically, the molten-salt titanium plating solution composition of the present disclosure contains fluoride ions and can therefore form a titanium plating film having high surface smoothness. In addition, the molten-salt titanium plating solution composition of the present disclosure contains, as cations, ions of at least one Group I metal selected from the group of lithium and sodium having a lower reduction potential (harder to reduce) than potassium, and the content of potassium ions in the plating solution composition is less than or equal to 5 mol%. In the condition where titanium plating is performed, metal fog is less likely to be generated from lithium ions and sodium ions. The content of potassium in the molten-salt titanium plating solution composition is sufficiently low. Therefore, generation of metal fog during plating can be suppressed. - [2] A ratio of the fluoride ions to all anions contained in the molten-salt titanium plating solution composition may be more than or equal to 30 mol% and less than or equal to 100 mol%. The molten-salt titanium plating solution composition containing fluoride ions at this ratio enables a titanium-plated member having a titanium plating film excellent in surface smoothness to be manufactured.
- [3] The molten-salt titanium plating solution composition may further contain chloride ions. The molten-salt titanium plating solution composition containing fluoride ions as well as chloride ions can be reduced in melting point by depression of melting point. As a result, a titanium plating film can be formed at a lower temperature.
- [4] The molten-salt titanium plating solution composition may contain more than or equal to 30 mol% and less than or equal to 50 mol% of the fluoride ions, with respect to 100 mol% of a total of the chloride ions and the fluoride ions. The content falling in this range enables further reduction of the melting point of the molten-salt titanium plating solution composition. As a result, a titanium plating film can be formed at a still lower temperature.
- [5] The molten-salt titanium plating solution composition preferably contains more than or equal to 0.1 mol% and less than or equal to 12 mol% of the titanium ions with respect to 100 mol% of all cations contained in the molten-salt titanium plating solution composition. Accordingly, a titanium plating film having high surface smoothness can be formed with a high yield.
- [6] The molten-salt titanium plating solution composition is used for manufacturing an insoluble electrode. Thus, an insoluble electrode having a titanium plating film excellent in surface smoothness can be manufactured.
- [7] The molten-salt titanium plating solution composition is used for manufacturing a current collector. Thus, a current collector having a titanium plating film excellent in surface smoothness can be manufactured.
- [8] The molten-salt titanium plating solution composition is used for manufacturing a biomaterial. Thus, a biomaterial having a titanium plating film excellent in surface smoothness can be manufactured. Such a biomaterial can also be excellent in corrosion resistance.
- [9] According to an aspect of the present disclosure, a method for manufacturing a titanium-plated member includes: preparing a substrate having an electrically conductive surface; immersing the substrate in the above-described molten-salt titanium plating solution composition; and forming a titanium plating film on the surface of the substrate by applying electric current to cause the substrate immersed in the molten-salt titanium plating solution composition to serve as a cathode and cause the surface of the substrate to be coated with titanium. Thus, a titanium-plated member having a titanium plating film with high surface smoothness can be manufactured while generation of metal fog is suppressed.
- Next, an embodiment of a molten-salt titanium plating solution composition and a method for manufacturing a titanium-plated member in the present disclosure is described in detail in the following. The expression "A to B" herein specifies an upper limit and a lower limit of a range (i.e., more than or equal to A and less than or equal to B). In the case where A is not accompanied by a unit but only B is accompanied by a unit, the unit for B is identical to the unit for A.
- A molten-salt titanium plating solution composition in the present embodiment contains ions of at least one Group I metal selected from the group of lithium (Li+) and sodium (Na+), fluoride ions (F-), and titanium ions (Tin+ (n is an integer of 2 or more and 4 or less, the same applies as well to the following)). The plating solution composition contains less than or equal to 5 mol% of potassium ions (K+) with respect to 100 mol% of all ion components contained in the plating solution composition.
- Preferably, the plating solution composition further contains chloride ions (Cl-).
- The plating solution composition can be prepared as a molten salt by dissolving a titanium compound serving as a source of Tin+ in a mixture of at least one of lithium fluoride (LiF) and sodium fluoride (NaF) and at least one of lithium chloride (LiCl) and sodium chloride (NaCl), for example. In this case, the plating solution composition may contain, as Tin+ in a titanium compound, multiple types of titanium that are different in valence.
- Examples of the titanium compound serving as a source of Tin+ may include hexafluorotitanic acid (H2TiF6), potassium hexafluorotitanate (K2TiF6), ammonium hexafluorotitanate ((NH4)2TiF6), sodium hexafluorotitanate (Na2TiF6), potassium titanium oxalate dihydrate (K2TiO(C2O4)2 • 2H2O), titanium chloride (III)(TiCl3), titanium chloride (IV)(TiCl4), and the like. Potassium hexafluorotitanate (K2TiF6) and potassium titanium oxalate dihydrate (K2TiO(C2O4)2 • 2H2O) contain potassium ions, and therefore, these titanium compounds are used at respective contents so that the K+ content with respect to 100 mol% of all ion components contained in the plating solution composition is less than or equal to 5 mol%, or these titanium compounds are used together with another titanium compound (such as titanium chloride (IV) or the like, for example) that generates no K+.
- In the plating solution composition that is a molten salt, LiF, NaF, LiCl, and NaCl are ionized to be present in the form of Li+, Na+, F-, and Cl-. The titanium compound is also ionized to be present in the form of Tin+. It is preferable to prepare, as a molten salt, a plating solution composition containing: ions of at least one Group I metal selected from the group of Li+ and Na+; F-; Cl-; and Tin+ in this way.
- The fact that Li+, Na+, F-, Cl-, and Tin+ are present in the plating solution composition of the present embodiment can be confirmed, for example, by dissolving the plating solution composition in a solution of a mixture of nitric acid and hydrofluoric acid, and analyzing the solution by ICP (Inductively Coupled Plasma Spectrometry) or IC analysis (Ion Chromatography). As an ICP apparatus, iCAP6200 or the like manufactured by Thermo Fisher Scientific Inc. may be used, for example.
- The ratio of the fluoride ions to all anions contained in the molten-salt titanium plating solution composition may be more than or equal to 30 mol% and less than or equal to 100 mol%. The molten-salt titanium plating solution composition containing fluoride ions at such a ratio enables manufacture of a titanium-plated member having a titanium plating film excellent in surface smoothness. The ratio of fluoride ions to all anions is preferably more than or equal to 40 mol% and less than or equal to 90 mol%, and more preferably more than or equal to 45 mol% and less than or equal to 75 mol%.
- Preferably, the content of F- with respect to 100 mol% of a total of Cl- and F- is more than or equal to 30 mol% and less than or equal to 50 mol%. When the ratio of Cl- relative to F- is increased, the melting point of the plating solution composition is once reduced by depression of melting point, and thereafter increased again. The melting point depression effect is large when the ratio of the F- content relative to 100 mol% of the total content of Cl- and F- falls in a predetermined range. Specifically, reduction of the melting point is large when the content of F- with respect to 100 mol% of the total of Cl- and F- is more than or equal to 30 mol% and less than or equal to 50 mol%, which facilitates plating at a lower temperature. More preferably, the content of F- with respect to 100 mol% of the total of Cl- and F- is more than or equal to 30 mol% and less than or equal to 45 mol%, because reduction of the melting point is larger.
- The content of Tin+ in the plating solution composition is not particularly limited, but set appropriately depending on plating conditions. However, an excessively high content of Tin+ may cause unnecessary precipitates to be formed, which increases reduction of current efficiency. In contrast, an excessively low content of Tin+ does not allow a titanium plating film to be formed sufficiently. The content of Tin+ is therefore preferably less than or equal to 20 mol% and more preferably less than or equal to 12 mol%, with respect to 100 mol% of all cations in the plating solution composition. The content of Tin+ is preferably more than or equal to 0.1 mol%, and more preferably more than or equal to 0.5 mol%, with respect to 100 mol% of all cations in the plating solution composition. In other words, the content of titanium ions with respect to 100 mol% of all cations contained in the molten-salt titanium plating solution composition is preferably more than or equal to 0.1 mol% and less than or equal to 12 mol%.
- Next, referring to
Figs. 1 to 3 , a method for manufacturing a titanium-plated member in the present embodiment is described.Fig. 1 is a schematic cross-sectional view showing an example of a part of a titanium-plated member.Fig. 2 is a flowchart showing a procedure for manufacturing a titanium-plated member.Fig. 3 is a schematic cross-sectional view showing an example of a state in which a substrate is immersed in a molten-salt titanium plating solution composition. - Referring to
Fig. 1 , a titanium-platedmember 1 is made up of asubstrate 10 and a titanium plating film 20 (hereinafter also referred to simply as "platingfilm 20") formed on a surface ofsubstrate 10. Platingfilm 20 is a film made of titanium. Referring toFigs. 2 and3 , titanium-platedmember 1 is manufactured through steps S10 to S40 shown inFig. 2 . A method for manufacturing titanium-platedmember 1 according to the present embodiment includes: the step of preparingsubstrate 10 having an electrically conductive surface (S10); the step of immersingsubstrate 10 in plating solution composition 50 (S20); and the step of formingtitanium plating film 20 on the surface ofsubstrate 10 by applying electric current to causesubstrate 10 immersed in platingsolution composition 50 to serve as a cathode and cause the surface ofsubstrate 10 to be coated with titanium (S30). Further, the method for manufacturing titanium-platedmember 1 preferably includes the step of cleaning a surface of plating film 20 (S40). The method for manufacturing titanium-platedmember 1 of the present embodiment may include any step besides the steps S10, S20, S30, and S40. In the following, each of these steps is described. - First,
substrate 10 having an electrically conductive surface is prepared (S10). Thematerial forming substrate 10 is not particularly limited as long as the material has an electrically conductive surface. Examples ofsubstrate 10 include, for example, a substrate made of iron or nickel, a substrate made of an alloy of them, or a multilayer substrate having a surface made of a layer of iron or nickel or an alloy thereof. - The shape of
substrate 10 is not particularly limited. For example,substrate 10 in the shape of any of various shapes such as plate, column, pipe, mesh, or the like may be employed assubstrate 10. - Next,
substrate 10 is immersed in plating solution composition 50 (S20). As platingsolution composition 50, a plating solution composition prepared in the above-described way is used. - Referring to
Fig. 3 , in the present embodiment, platingsolution composition 50 contains ions of at least one Group I metal selected from the group of lithium (Li+) and sodium (Na+), fluoride ions (F-), titanium ions (Tin+), and chloride ions (Cl-). Further, platingsolution composition 50 is prepared so that the content of potassium ions (K+) with respect to 100 mol% of all ion components contained in platingsolution composition 50 is less than or equal to 5 mol%. - In the present embodiment, preferably plating
solution composition 50 is prepared so that the ratio of the fluoride ions to all anions contained in the molten-salt titanium plating solution composition is more than or equal to 30 mol% and less than or equal to 100 mol%. Further, preferably platingsolution composition 50 is prepared so that platingsolution composition 50 contains more than or equal to 30 mol% and less than or equal to 50 mol% of F-, with respect to 100 mol% of the total of Cl- and F-. Preferably platingsolution composition 50 is prepared so that platingsolution composition 50 contains more than or equal to 0.1 mol% and less than or equal to 12 mol% of Tin+ with respect to 100 mol% of all cations contained in platingsolution composition 50. - Next, electric current is applied to cause
substrate 10 immersed in platingsolution composition 50 to serve as a cathode, and cause the surface ofsubstrate 10 to be coated with titanium, to thereby formtitanium plating film 20 on this surface (S30). The step of formingplating film 20 is performed in the following way. Withsubstrate 10 immersed in platingsolution composition 50, electric current is applied by applying a voltage between ananode 30 andsubstrate 10 serving as a cathode that are immersed in platingsolution composition 50 to cause electrolysis of platingsolution composition 50. Accordingly, on the surface ofsubstrate 10 serving as a cathode, titanium ions are reduced to titanium and the surface ofsubstrate 10 is coated with titanium. Thus, platingfilm 20 is formed on the surface ofsubstrate 10. - Electrolysis of plating
solution composition 50 is preferably performed so that the absolute value of the current density, onsubstrate 10, of current flowing betweenanode 30 andsubstrate 10 is more than or equal to 1 mA/cm2 and less than or equal to 500 mA/cm2, and more preferably performed so that the absolute value of the current density is more than or equal to 1 mA/cm2 and less than or equal to 300 mA/cm2. When electrolysis of platingsolution composition 50 is performed so that the absolute value of the current density of current flowing betweenanode 30 andsubstrate 10 is more than or equal to 1 mA/cm2, platingfilm 20 can be formed on the surface ofsubstrate 10 in a shorter time. When electrolysis of platingsolution composition 50 is performed so that the absolute value of the current density of current flowing betweenanode 30 andsubstrate 10 is less than or equal to 500 mA/cm2, particularly less than or equal to 300 mA/cm2, platingfilm 20 having higher surface smoothness can be formed. - Finally, the surface of plating
film 20 is cleaned (S40). On the surface of platingfilm 20 thus formed, components contained in platingsolution composition 50 remain. Therefore, a cleaning agent can be used to clean the surface of platingfilm 20 to thereby remove the components remaining on the surface of platingfilm 20. As the cleaning agent, water may be used. In other words,substrate 10 on whichplating film 20 is formed may be cleaned with water. Further, in order to remove a substance such as poorly water-soluble substance that is difficult to remove with only water, a cleaning agent other than water may be used such as a cleaning agent containing water-soluble salt having a high compatibility with components contained in platingsolution composition 50, instead of or in combination with water. In this way, titanium-platedmember 1 having a surface ofsubstrate 10 coated with platingfilm 20 is manufactured. - Titanium-plated
member 1 manufactured in this way can be used in a variety of fields, as a member having a protective film with a high hardness and a high surface smoothness as well as excellent corrosion resistance and excellent wear resistance. - The ratio of average surface roughness Ra to average thickness R of plating film 20 ((Ra/R) × 100 (%)) of titanium-plated
member 1 manufactured by the above-described method is preferably less than or equal to 10%, and more preferably less than or equal to 5%. With the ratio falling in this range, titanium-platedmember 1 havingplating film 20 with a sufficiently high surface smoothness can be provided. - Average surface roughness Ra of plating
film 20 can be measured through observation of a cross section with an SEM (Scanning Electron Microscope) or by means of a surface roughness meter. Average thickness R of platingfilm 20 can be determined through observation of a cross section with an SEM. Average surface roughness Ra of platingfilm 20 refers to an arithmetic mean roughness Ra specified under JIS B 0601 (2001). Average thickness R of platingfilm 20 may be an arithmetic mean thickness of platingfilm 20 determined from thicknesses at any 10 points on an SEM image, for example. - Preferably, the molten-salt titanium plating solution composition is used for manufacturing an insoluble electrode. With such a molten-salt titanium plating solution composition for manufacturing an insoluble electrode, an insoluble electrode having a titanium plating film excellent in surface smoothness can be manufactured.
- Preferably, the insoluble electrode is used for manufacturing hydrogen. When the insoluble electrode is used for manufacturing hydrogen, the electrode can be provided as a hydrogen-manufacturing insoluble electrode with a low resistance. Accordingly, hydrogen with a high purity can be manufactured.
- Preferably, the molten-salt titanium plating solution composition is used for manufacturing a current collector. With such a current-collector-manufacturing molten-salt titanium plating solution composition, a current collector having a titanium plating film with excellent surface smoothness can be manufactured.
- Preferably, the current collector is used for a fuel cell. A current collector for a fuel cell can be provided as a fuel-cell current collector having a good electrical conductivity. Particularly when the current collector is used for a fuel cell, the current collector is more preferably used for a polymer electrolyte fuel cell.
- Preferably, the molten-salt titanium plating solution composition is used for manufacturing a biomaterial. With such a biomaterial-manufacturing molten-salt titanium plating solution composition, a biomaterial having a titanium plating film with an excellent surface smoothness can be manufactured. This biomaterial is also excellent in corrosion resistance.
- The use of the biomaterial is preferably selected from the group consisting of spinal fixation device, fracture fixation device, artificial joint, artificial heart valve, intravascular stent, denture base, artificial dental root, and orthodontic wire.
- As seen from the above, molten-salt titanium
plating solution composition 50 according to the present embodiment enables generation of metal fog during plating to be suppressed. Further, in accordance with the method for manufacturing titanium-platedmember 1, titanium-platedmember 1 havingplating film 20 with high surface smoothness can be manufactured. - In the above description of the embodiment, molten-salt titanium
plating solution composition 50 containing chloride ions (Cl-) is described. Molten-salt titaniumplating solution composition 50, however, may be prepared without containing Cl-. As a molten-salt titaniumplating solution composition 50 containing no Cl-, molten-salt titaniumplating solution composition 50 can be prepared to contain other anions instead of Cl-. In this case, the aforementioned other anions are preferably selected that are stable at the plating temperature and will not form a residue such as salt that is difficult to remove after plating. - Preferably, as the molten-salt titanium plating solution composition, plating
solution composition 50 is prepared to contain more than or equal to 30 mol% and less than or equal to 50 mol% of F- with respect to 100 mol% of the total of Cl- and F-, and contain more than or equal to 0.1 mol% and less than or equal to 12 mol% of Tin+ with respect to 100 mol% of all cations contained in platingsolution composition 50. The limitations on respective contents are not requisite ones. The contents can be set appropriately in consideration of the required plating temperature and plating performance. - The above-described embodiments are hereinafter described more specifically with reference to Examples. The present disclosure is not limited to these Examples. In Table 1, Experiment No. 1 is an example where a plating solution composition of an Example within the range of the molten-salt titanium plating solution composition of the present disclosure was used. Experiment Nos. 2 to 4 are each an example where a plating solution composition of a comparative example out of the range of the molten-salt titanium plating solution composition of the present disclosure was used.
- Molten-salt titanium plating solution compositions of Experiment Nos. 1 to 4 were each prepared by dissolving, in the main agent for the plating solution composition shown in Table 1, one or both of K2TiF6 powder and TiCl4 gas as a titanium source at a ratio of 2 mol of the total of one or both of K2TiF6 powder and TiCl4 gas with respect to 100 mol of the main agent. Further, through the steps S10 to S40 of the method for manufacturing a titanium-plated member as described above (see
Fig. 2 ), each of the molten-salt titanium plating solution compositions of Experiment Nos. 1 to 4 was used to plate a surface of a respective substrate (made of nickel, 0.1 mm in thickness, 5 mm × 25 mm in size). In this way, titanium-plated members of Experiment Nos. 1 to 4 were produced. Subsequently, for each of the titanium-plated members of Experiment Nos. 1 to 4, the plating performance was evaluated. Further, whether or not metal fog was generated in the process of performing titanium plating for each of Experiment Nos. 1 to 4 was confirmed by visual inspection. The results are shown in Table 1. As to the evaluation of the plating performance, specifically the ratio of an abnormal plating portion resulting from discoloration of the plated surface and/or lack of plating on the surface to be plated, for example, was evaluated based on the area ratio (%) of the abnormal plating portion. In Table 1, the level of the plating performance is classified into those termed "good," "average," "somewhat poor" and "poor" respectively. "Good" means that the abnormal portion is less than 5%, "average" means that the abnormal portion is more than or equal to 5% and less than 20 %, "somewhat poor" means that the abnormal portion is more than or equal to 20% and less than 50%, and "poor" means that the abnormal portion is more than or equal to 50%. In Table 1, as to whether or not metal fog was generated, "small amount was generated" means that white smoke was confirmed during cleaning with water, and "generated" means that white smoke and sparks were confirmed.[Table 1] Experiment No. 1 2 3 4 main agent LiF-LiCl LiF-KCl LiF-NaF-KF KF-KCl makeup of plating solution composition (molar ratio) LiF 45 45 46.5 0 LiCl 55 0 0 0 NaF 0 0 11.5 0 KF 0 0 42 45 KCl 0 55 0 55 K2TiF6 2 1 1 2 TiCl 40 1 1 0 ratio of K+ (mol%) to 100 mol% of all ion components 1.8 27 21 48 F-/(Cl-+F-) (mol%) 51 46 96 51 ratio of Tin+ (mol%) to 100 mol% of all cations 1.9 1.9 1.9 1.9 plating temperature (°C) 650 350 to 500 600 to 700 650 plating performance good poor good good generation of metal fog no metal fog was generated small amount was generated generated generated - As shown in Table 1, as to Experiment No. 1, the plating performance was good and generation of metal fog was not confirmed. Thus, generation of metal fog of potassium could be suppressed by performing titanium plating using a molten-salt titanium plating solution composition in which the content of K+ with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition was less than or equal to 5 mol%. The plating performance was also good in the case of a molten-salt titanium plating solution composition containing K+ at a smaller content and containing Li+ as main cations instead.
- In contrast, as to Experiment No. 2, poor plating performance and generation of a small amount of metal fog were confirmed. As to Experiment Nos. 3 and 4, while the plating performance was good, generation of metal fog was confirmed. Thus, metal fog of potassium was generated in the case of a molten-salt titanium plating solution composition in which the content of K+ with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition was more than 5 mol%.
- Molten-salt titanium plating solution compositions of Experiment Nos. 5 to 16 were each prepared by dissolving, in the main agent for the plating solution composition shown in Tables 2 to 4, one or both of K2TiF6 powder and TiCl4 gas as a titanium source at the ratio shown in Tables 2 to 4 with respect to 100 mol of the main agent.
- The molten-salt titanium plating solution composition of Experiment No. 5 contains more than 5 mol% of K+ with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition, and is therefore a Comparative Example. Respective molten-salt titanium plating solution compositions of Experiment Nos. 6 to 16 each contain less than or equal to 5 mol% of K+ with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition, and are therefore Examples.
- Respective molten-salt titanium plating solution compositions of Experiment Nos. 7 and 15 are Examples containing no chloride ions. Respective molten-salt titanium plating solution compositions of Experiment No. 8, Nos. 10 to 12, and No. 16 are Examples in which the content of fluoride ions with respect to 100 mol% of the total of chloride ions and fluoride ions is more than or equal to 30 mol% and less than or equal to 50 mol%. It should be noted that the molten-salt titanium plating solution composition of Experiment No. 12 contains more than 12 mol% of titanium ions with respect to 100 mol% of all cations contained in the molten-salt titanium plating solution composition. The molten-salt titanium plating solution composition of Experiment No. 16 contains less than 0.1 mol% of titanium ions with respect to 100 mol% of all cations contained in the molten-salt titanium plating solution composition.
- Next, each of the molten-salt titanium plating solution compositions of Experiment Nos. 5 to 16 was used to plate a surface of a respective substrate (made of nickel, 0.1 mm in thickness, 5 mm × 25 mm in size) with titanium through the steps S10 to S40 of the method for manufacturing a titanium-plated member as described above (see
Fig. 2 ). Thus, titanium-plated members of Experiment Nos. 5 to 16 were manufactured. Further, as to the titanium-plated members of Experiment Nos. 5 to 16, the plating performance was evaluated by the same evaluation method as Example 1. As to the titanium-plated members of Experiment Nos. 5 to 16, whether or not metal fog was generated in the process of titanium plating was also confirmed by the same evaluation method as Example 1. The results are shown in Tables 2 to 4. - The correlations between respective molten-salt titanium plating solution compositions of Experiment Nos. 5 to 16 and respective titanium-plated members of Experiment Nos. 5 to 16 are as follows. Specifically, a titanium-plated member produced using the molten-salt titanium plating solution composition of Experiment No. 5 corresponds to the titanium-plated member of Experiment No. 5. The same applies as well to the subsequent Experiments, i.e., a titanium-plated member produced using a molten-salt titanium plating solution composition of Experiment No. "X" corresponds to a titanium-plated member of Experiment No. "X" (X is an arbitrary numeral).
[Table 2] Experiment No. 5 6 7 8 main agent LiF-KCl-KF LiF-KCl-KF LiF LiF-LiCl makeup of plating solution composition (molar ratio) LiF 45 45 100 30 LiCl 55 55 0 70 NaF 0 0 0 0 KF 8 6 0 0 KCl 0 0 0 0 K2TiF6 2 2 2 2 TiCl4 0 0 0 0 ratio of K+ (mol%) to 100 mol% of all ion components 5.1 4.3 1.8 1.8 F-/(Cl-+F-) (mol%) 54 53 100 38 ratio of Tin+ (mol%) to 100 mol% of all cations 1.8 1.8 1.9 1.9 plating temperature (°C) 650 650 900 650 plating performance good good good good generation of metal fog small amount was generated not generated not generated not generated [Table 3] Experiment No. 9 10 11 12 main agent LiF-LiCl LiF-LiCl LiF-LiCl LiF-NaCl makeup of plating solution composition (molar ratio) LiF 50 50 50 40 LiCl 50 50 50 0 NaF 0 0 0 0 KF 8 0 0 0 KCl 0 0 0 0 K2TiF6 2 0 0 2 TiCl4 0 13 14 0 NaCl 0 0 0 60 ratio of K+ (mol%) to 100 mol% of all ion components 1.8 0 0 1.8 F-/(Cl-+F-) (mol%) 55 33 32 46 ratio of Tin+ (mol%) to 100 mol% of all cations 1.9 11.5 12.3 1.9 plating temperature (°C) 650 650 650 750 plating performance good good poor good generation of metal fog not generated not generated not generated not generated [Table 4] Experiment No. 13 14 15 16 main agent LiF-LiCl LiF-LiCl LiF-NaF LiF-LiCl makeup of plating solution composition (molar ratio) LiF 20 60 30 45 LiCl 80 40 0 55 NaF 0 0 70 0 KF 0 0 0 0 KCl 0 0 0 0 K2TiF6 2 2 2 0.03 TiCl4 0 0 0 0 ratio of K+ (mol%) to 100 mol% of all ion components 1.8 1.8 1.8 0.03 F-/(Cl-+F-) (mol%) 29 64 100 45 ratio of Tin+ (mol%) to 100 mol% of all cations 1.9 1.9 1.9 0.03 plating temperature (°C) 700 750 700 650 plating performance somewhat good good poor generation of metal fog not generated not generated not generated not generated - As shown in Tables 2 to 4, in the case of the molten-salt titanium plating solution composition of Experiment No. 5 containing more than 5 mol% of K+ with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition, metal fog of potassium was generated. In contrast, in the case of the molten-salt titanium plating solution compositions of Experiment Nos. 6 to 16 containing less than or equal to 5 mol% of K+ with respect to 100 mol% of all ion components, it was confirmed that no metal fog of potassium was generated.
- As seen from the above, molten-salt titanium
plating solution composition 50 and the method for manufacturing titanium-platedmember 1 according to the present embodiment enable generation of metal fog during plating to be suppressed. - The corrosion resistance of the following Ti-plated product to physiological saline solution was evaluated through the following procedure.
- The molten-salt titanium plating solution composition of Experiment No. 8 was used and, through the steps S10 to S40 of the method for manufacturing a titanium-plated member described above (see
Fig. 2 ), the surface of a nickel porous substrate (3 cm × 5 cm × 1 mmt, porosity: 96%, average pore size: 300 µm, hereinafter referred to as "nickel porous material") was plated with titanium. Thus, a Ti-plated product to serve as a specimen of an Example was prepared. - In contrast, as specimens of a comparative example, a Ni porous material (product name: "Celmet®" manufactured by Sumitomo Electric Industries, Ltd.) and a Ti metal sheet (manufactured by Nilaco Corporation) were prepared.
- Cyclic voltammetry was conducted under the following conditions. The results are shown in
Fig. 4 . InFig. 4 , the specimen of the Example and the specimens of the Comparative Example (Ni porous material and Ti metal sheet) are expressed as "Ti-plated product," "Ni" and "Ti" respectively. -
- electrolyte: 0.9 mass% sodium chloride aqueous solution (physiological saline solution)
- working electrode: specimen of Example or specimen of Comparative Example (Ti-plated product, Ni, or Ti)
- reference electrode: Ag/AgCl electrode
- counter electrode: Ni metal sheet
- scan rate: 10 mV/sec
- solution temperature: 25°C
- It has been proved from the results in
Fig. 4 that the Ti-plated product of the Example is lower in corrosion current density than the Ni porous material of the Comparative Example, and is thus stable in an environment of physiological saline solution. It is seen from this result that the Ti-plated product of the Example is suitable as a biomaterial. Further, the Ti-plated product of the Example is lower in corrosion current density than the Ti metal sheet of the Comparative Example. It is seen from this result that the structure of a metal porous material instead of a metal sheet is used to further improve the stability in an environment of physiological saline solution. - The corrosion resistance of the following Ti-plated product to saline solution simulating seawater was evaluated through the following procedure.
- As a specimen of the Example, a Ti-plated product manufactured by the same method as the Ti-plated product used for Example 3 was prepared. As a specimen of the Comparative Example, a Ti metal sheet (manufactured by Nilaco Corporation) was prepared.
- Cyclic voltammetry was conducted under the same conditions as those indicated above in the section [Corrosion resistance to physiological saline solution], except that 3.3 mass% saline solution simulating seawater was used as electrolyte. The results are shown in
Fig. 5 . InFig. 5 , the specimen of the Example and the specimen of the Comparative Example are expressed as "Ti-plated product" and "Ti commercial product" respectively. - It has been proved from the results in
Fig. 5 that the Ti-plated product of the Example is lower in current density than the Ti commercial product of the Comparative Example, and thus exhibits high corrosion resistance to seawater. It is seen from the above that the Ti-plated product of the Example is promising as an insoluble electrode (anode) for electrolysis of salt. - The suitability of the following Ti-plated product for polymer electrolyte fuel cell was evaluated through the following procedure.
- As a specimen of the Example, a Ti-plated product manufactured by the same method as the Ti-plated product used in Example 3 was prepared. As specimens of the Comparative Example, an Ni porous material (product name: "Celmet®" manufactured by Sumitomo Electric Industries, Ltd.) and a Ti metal sheet (manufactured by Nilaco Corporation) were prepared.
- Cyclic voltammetry was conducted under the same conditions as those indicated above in the section [Corrosion resistance to physiological saline solution], except that 10 mass% sodium nitrate aqueous solution (adjusted to pH = 3 by adding nitric acid) (simulated PEFC electrolyte) was used as electrolyte. The results are shown in
Figs. 6 and 7 . InFigs. 6 and 7 , the specimen of the Example and the specimens (Ni porous material and Ti metal sheet) of the Comparative Example are expressed as "Ti-plated product," "comparative Ni" and "comparative Ti" respectively. InFig. 6 , respective plots for "Ti-plated product" and "comparative Ti" depicting a correlation between the potential and the current density of the electrode overlap each other, and therefore,Fig. 7 shows these plots by expanding the scale of the vertical axis (current density) so that the plot depicting the correlation for "Ti-plated product" can be distinguished from the plot depicting the correlation for "comparative Ti." - It has been proved from the results in
Figs. 6 and 7 that the Ti-plated product for the Example is lower in current density than the comparative Ni of the Comparative Example, and therefore promising as a current collector material to be used for a polymer electrolyte fuel cell. - It should be construed that the embodiments and examples disclosed herein are given by way of illustration in all respects, not by way of limitation in any aspect. It is intended that the scope of the present invention is defined by claims, not by the description above, and encompasses all modifications and variations equivalent in meaning and scope to the claims.
- 1 titanium-plated member; 10 substrate; 20 plating film; 30 anode; 40 container; 50 plating solution composition
Claims (9)
- A molten-salt titanium plating solution composition comprising:ions of at least one Group I metal selected from the group of lithium and sodium;fluoride ions; andtitanium ions,the molten-salt titanium plating solution composition containing less than or equal to 5 mol% of potassium ions with respect to 100 mol% of all ion components contained in the molten-salt titanium plating solution composition.
- The molten-salt titanium plating solution composition according to claim 1, wherein a ratio of the fluoride ions to all anions contained in the molten-salt titanium plating solution composition is more than or equal to 30 mol% and less than or equal to 100 mol%.
- The molten-salt titanium plating solution composition according to claim 1 or 2, further comprising chloride ions.
- The molten-salt titanium plating solution composition according to claim 3, wherein the molten-salt titanium plating solution composition contains more than or equal to 30 mol% and less than or equal to 50 mol% of the fluoride ions, with respect to 100 mol% of a total of the chloride ions and the fluoride ions.
- The molten-salt titanium plating solution composition according to any one of claims 1 to 4, wherein the molten-salt titanium plating solution composition contains more than or equal to 0.1 mol% and less than or equal to 12 mol% of the titanium ions with respect to 100 mol% of all cations contained in the molten-salt titanium plating solution composition.
- The molten-salt titanium plating solution composition according to any one of claims 1 to 5, wherein the molten-salt titanium plating solution composition is used for manufacturing an insoluble electrode.
- The molten-salt titanium plating solution composition according to any one of claims 1 to 5, wherein the molten-salt titanium plating solution composition is used for manufacturing a current collector.
- The molten-salt titanium plating solution composition according to any one of claims 1 to 5, wherein the molten-salt titanium plating solution composition is used for manufacturing a biomaterial.
- A method for manufacturing a titanium-plated member, the method comprising:preparing a substrate having an electrically conductive surface;immersing the substrate in a molten-salt titanium plating solution composition according to any one of claims 1 to 5; andforming a titanium plating film on the surface of the substrate by applying electric current to cause the substrate immersed in the molten-salt titanium plating solution composition to serve as a cathode and cause the surface of the substrate to be coated with titanium.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2017100757 | 2017-05-22 | ||
| PCT/JP2018/009739 WO2018216320A1 (en) | 2017-05-22 | 2018-03-13 | Molten salt titanium plating solution composition and method for manufacturing titanium-plated member |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3633076A1 true EP3633076A1 (en) | 2020-04-08 |
| EP3633076A4 EP3633076A4 (en) | 2021-03-03 |
Family
ID=64395403
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP18806263.2A Withdrawn EP3633076A4 (en) | 2017-05-22 | 2018-03-13 | FELT SALT TITANIUM PLATING SOLUTION COMPOSITION AND METHOD FOR MANUFACTURING A TITANIUM-COATED ELEMENT |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20200080216A1 (en) |
| EP (1) | EP3633076A4 (en) |
| JP (1) | JP6947212B2 (en) |
| KR (1) | KR20200010199A (en) |
| CN (1) | CN110582594A (en) |
| WO (1) | WO2018216320A1 (en) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2019171744A1 (en) * | 2018-03-08 | 2019-09-12 | 住友電気工業株式会社 | Method for manufacturing titanium-plated member, and titanium-plated member |
| JP7207411B2 (en) * | 2018-07-18 | 2023-01-18 | 住友電気工業株式会社 | Method for evaluating electrolyte for titanium plating and method for manufacturing titanium-plated member using electrolyte for titanium plating |
| JP7489309B2 (en) | 2020-12-24 | 2024-05-23 | 東邦チタニウム株式会社 | Manufacturing method of titanium plated material |
| US20260117409A1 (en) * | 2024-01-17 | 2026-04-30 | Battelle Memorial Institute | Composition for plating metal coatings and methods of making and using the same |
Family Cites Families (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3479159A (en) * | 1966-11-10 | 1969-11-18 | Gen Electric | Process for titaniding base metals |
| US3979267A (en) * | 1972-01-24 | 1976-09-07 | Townsend Douglas W | Electrolytic method |
| JPS5417304B2 (en) * | 1974-04-18 | 1979-06-28 | ||
| JPS51138511A (en) * | 1975-05-27 | 1976-11-30 | Sony Corp | Method for regulating the hardness of metallic tita nium |
| US4483752A (en) * | 1982-09-28 | 1984-11-20 | Eltech Systems Corporation | Valve metal electrodeposition onto graphite |
| JPH06173065A (en) * | 1992-12-09 | 1994-06-21 | Japan Energy Corp | Method for purifying Ti |
| JP3779368B2 (en) * | 1996-02-09 | 2006-05-24 | 松田医科工業株式会社 | Biological composite implant material |
| JP2000256898A (en) * | 1999-03-03 | 2000-09-19 | Permelec Electrode Ltd | Copper plating method of wafer |
| DE112005002435B4 (en) * | 2004-10-01 | 2014-01-02 | Kyoto University | Molten salt bath, deposit obtained using the molten salt bath, production process for a metal product and metal product |
| US9512530B2 (en) * | 2004-11-24 | 2016-12-06 | Sumitomo Electric Industries, Ltd. | Molten salt bath, deposit, and method of producing metal deposit |
| JP4919225B2 (en) * | 2007-02-02 | 2012-04-18 | 住友電気工業株式会社 | Electrode for electric double layer capacitor |
| JP2013147731A (en) * | 2011-12-22 | 2013-08-01 | Sumitomo Electric Ind Ltd | Molten salt electrolysis metal fabrication method |
| CN103882477B (en) * | 2012-12-21 | 2016-12-28 | 攀钢集团攀枝花钢铁研究院有限公司 | A kind of electrolyte for preparing Titanium and fused salt and the preparation method of Titanium |
| JP6405199B2 (en) | 2013-11-19 | 2018-10-17 | 住友電気工業株式会社 | Electrodeposition electrolyte and method for producing metal film |
| CN105112963B (en) * | 2015-10-10 | 2017-10-24 | 东北大学 | A kind of method that utilization fused salt electrodeposition process prepares metallic aluminium and its alloy |
| JP6518577B2 (en) | 2015-11-30 | 2019-05-22 | 株式会社吉野工業所 | Coating container which measures and applies contents |
| EP3546621A4 (en) * | 2016-11-22 | 2020-08-05 | Sumitomo Electric Industries, Ltd. | TITANIUM PLATE SOLUTION MANUFACTURING METHOD AND TITANIUM PLATED PRODUCT MANUFACTURING METHOD |
| WO2019171744A1 (en) * | 2018-03-08 | 2019-09-12 | 住友電気工業株式会社 | Method for manufacturing titanium-plated member, and titanium-plated member |
-
2018
- 2018-03-13 WO PCT/JP2018/009739 patent/WO2018216320A1/en not_active Ceased
- 2018-03-13 CN CN201880025988.3A patent/CN110582594A/en active Pending
- 2018-03-13 KR KR1020197031022A patent/KR20200010199A/en not_active Withdrawn
- 2018-03-13 JP JP2019519485A patent/JP6947212B2/en active Active
- 2018-03-13 EP EP18806263.2A patent/EP3633076A4/en not_active Withdrawn
- 2018-03-13 US US16/603,920 patent/US20200080216A1/en not_active Abandoned
Also Published As
| Publication number | Publication date |
|---|---|
| US20200080216A1 (en) | 2020-03-12 |
| JP6947212B2 (en) | 2021-10-13 |
| JPWO2018216320A1 (en) | 2020-03-19 |
| KR20200010199A (en) | 2020-01-30 |
| EP3633076A4 (en) | 2021-03-03 |
| WO2018216320A1 (en) | 2018-11-29 |
| CN110582594A (en) | 2019-12-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6960095B2 (en) | Metal porous material, insoluble anode, fuel cell electrode, hydrogen production equipment, biomaterial, and metal porous material production method | |
| JP6960096B2 (en) | Composite metal porous material, insoluble anode, fuel cell electrode, hydrogen production equipment, shape memory alloy, biomaterial, and method for producing composite metal porous material. | |
| US20200080216A1 (en) | Molten-salt titanium plating solution composition and method for manufacturing titanium-plated member | |
| EP3633078A1 (en) | Method for producing titanium-plated member | |
| US4162204A (en) | Plated metallic cathode | |
| CN113463148A (en) | Method for electroplating gold on surface of titanium or titanium alloy substrate | |
| EA029324B1 (en) | Electrode for oxygen evolution in industrial electrochemical processes | |
| JP6802255B2 (en) | Conductive material and its manufacturing method | |
| Shekhanov et al. | Electrodeposition of tin–nickel alloys from oxalate–sulfate and fluoride–chloride electrolytes | |
| WO2022138219A1 (en) | Metal-filled microstructure and method for manufacturing metal-filled microstructure | |
| JP7086172B2 (en) | Titanium-plated member manufacturing method and titanium-plated member | |
| Liu et al. | Electrodeposition of molybdenum from water-in-acetate electrolytes | |
| US20220243338A1 (en) | Electrode coating | |
| JP6889447B2 (en) | Titanium plating solution manufacturing method and titanium plating product manufacturing method | |
| US20160298247A1 (en) | Amalgam electrode, method for manufacturing the same, and method for electrochemical reduction of carbon dioxide using the same | |
| JP7575445B2 (en) | Titanium plating electrolyte and method for manufacturing titanium-plated member using the titanium plating electrolyte | |
| JP2011208175A (en) | Method for producing plated article, and plated article | |
| EP4567160A1 (en) | Electroplate coating | |
| JP4632966B2 (en) | Method for producing electrolytic metal powder | |
| TW201518560A (en) | Electrolyte for electrodepositing molybdenum and method for forming molybdenum-containing layer | |
| EP4567153A1 (en) | Catalytic coating | |
| JP7516903B2 (en) | Aluminum foil manufacturing method | |
| KR102524705B1 (en) | Method of producing surface-treated steel sheet and surface-treated steel sheet | |
| KR20140061851A (en) | Method of forming tantalum alloy coating film by using molten salt multi-anode reactive alloy coating(marc) process and structure frame manufactured by the same | |
| KR20160060523A (en) | Method of forming tantalum coating film and structure frame manufactured by the same |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20190927 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20210128 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C25D 3/66 20060101AFI20210122BHEP |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN WITHDRAWN |
|
| 18W | Application withdrawn |
Effective date: 20240502 |