EP2785890B1 - Rail steel with an excellent combination of wear properties, rolling contact fatigue resistance and weldability - Google Patents
Rail steel with an excellent combination of wear properties, rolling contact fatigue resistance and weldability Download PDFInfo
- Publication number
- EP2785890B1 EP2785890B1 EP12791480.2A EP12791480A EP2785890B1 EP 2785890 B1 EP2785890 B1 EP 2785890B1 EP 12791480 A EP12791480 A EP 12791480A EP 2785890 B1 EP2785890 B1 EP 2785890B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- rail
- steel
- steel according
- content
- vanadium
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/12—Ferrous alloys, e.g. steel alloys containing tungsten, tantalum, molybdenum, vanadium, or niobium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/24—Ferrous alloys, e.g. steel alloys containing chromium with vanadium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/46—Ferrous alloys, e.g. steel alloys containing chromium with nickel with vanadium
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/04—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for rails
Definitions
- This invention relates to a rail steel, particularly for use as a grooved rail such as those used for tramway track, having an excellent combination of properties, in particular, the resistance to both wear and rolling contact fatigue and at the same time being capable of being weld restored without the need for high temperature preheat.
- Cost effectiveness of rail transport has become a significant issue in recent years.
- Replacing an embedded rail in a tramway network causes service disruptions; not only for the rail traffic, but also for other users of the shared infrastructure as such networks are installed in city centres.
- Tramway networks are often characterised by very tight track radii that inevitably experience high rates of side wear and hence can be the factor dictating rail life.
- a key first requirement of a cost effective rail steel grade for tramway applications is its ability to be weld restored without the need for high temperature preheat that damages the surrounding polymer in which the rail is embedded.
- the factor determining the life of the rail is the rate of vertical head wear and hence the second key requirement of a cost effective rail steel grade is its wear resistance.
- US2009/0134647 refers to a railroad wheel steel with a pearlitic structure, and contains (in weight%) carbon (0.65-0.80), silicon (0.90-1.10), manganese (0.85-1.15), phosphorus (0.001-0.030), niobium (0.009-0.013), sulfur (0.005-0.040) and remainder of iron and unavoidable impurities.
- the steel further contains chromium (0.10-0.25), nickel (0.050-0.150), molybdenum (0.20-0.30) and vanadium (0.10-0.30).
- RCF Rolling Contact Fatigue
- composition of the new rail steel needs to be designed to not only meet the requirements of resistance to wear, RCF, and corrugation but also to ensure that the transformation to martensite occurs over such a range that it prevents completion of transformation when using the low preheat weld restoration technology.
- the critical success factor for such a weld restoration process is the absence of any hard brittle microstructure or incipient cracks within the weld metal, weld metal-parent rail interface, or within the heat affected zone, all of which would subsequently lead to spalling of the deposit from the propagation of the incipient cracks through fatigue.
- One or more of the objects of the invention was achieved with a high-strength pearlitic rail steel having an excellent combination of wear properties, rolling contact fatigue resistance and weld restorability, containing (in weight %):
- Carbon is the most cost effective strengthening alloying element in rail steels as it provides the most cost effective addition to achieve the hardness and strength in fully pearlitic steels.
- the maximum value of carbon is 0.8%. This reduces the risk of formation of a cementite network at the grain boundaries. More preferably the range of carbon content is from 0.735% to 0.785%. This range provides the optimal balance between the volume fraction of hard cementite and the prevention of the formation of a deleterious network of embrittling cementite at grain boundaries.
- Carbon is also a potent hardenability agent that facilitates a lower transformation temperature and hence finer interlamellar spacing.
- the high volume fraction of hard cementite and fine interlamellar spacing provides the wear resistance and contributes towards the increased RCF resistance of the composition included in an embodiment of the invention. Furthermore, as demonstrated by the Tata Steel low preheat weld restoration process 1 , it is essential to lower the Martensite Start (Ms) temperature of the steel to ensure a robust weld deposit.
- Ms Martensite Start
- the prescribed range of carbon is essential to achieve this objective.
- the following widely accepted methodologies for the calculation of M s temperature clearly identify the efficacy of carbon in reducing the magnitude of this parameter. In effect, carbon is between 13 to 17 times more potent in reducing the M s temperature compared to manganese. According to Andrews (J. Iron & Steel Inst., 183 (1965), pp.
- the Martensite Start (M s ) temperature of the steel is below about 160°Cto ensure a robust weld deposit.
- the addition of Silicon is an integral and essential part of the design of the steel to engineer the resulting microstructure and properties and not, as in most other rail steels, a reflection of the manufacturing process route rather than an intentional alloying addition. Silicon is often used as a deoxidising element and as such the addition of silicon is usually intended for that purpose only.
- the microstructure contains little or no proeutectoid ferrite. Instead it is primarily the interlamellar spacing of the pearlite that dictates the resulting properties.
- the refinement of the pearlitic microstructure in grooved rail compositions has been achieved trough the use of accelerated cooling.
- the novelty of the approach in this invention is to treat the pearlitic microstructure as a three-dimensional entity in which the behaviour at the wheel-rail interface is governed by the properties of the two components of pearlite, ferrite and cementite laths, rather than just the bulk properties of hardness and tensile strength. Consequently, the novelty in this invention lies in the use of silicon to strengthen the pearlitic ferrite through solid solution strengthening which in turn imparts an increased resistance to ratchetting, wear, and rolling contact fatigue. A minimum Silicon content of 0.65% is essential for the steel according to the invention to attain the required mechanical property values, wear resistance and RCF resistance.
- Silicon additions have a very limited effect on hardenability of steel and this is reflected in the equations for the calculation of M s temperature, the addition of up to 1.0% Silicon is acknowledged to make a small contribution to the lowering of the M s temperature. Silicon content between 0.65% and 0.80% was found to provide a good balance of the required mechanical properties without any adverse effect on weld restorability.
- Manganese is a key alloying element in all grooved rail steels to provide the required hardenability to ensure a relatively fine interlamellar spacing following natural or accelerated cooling of such steels. This purpose remains valid for the current invention. In the current invention, which does not rely on accelerated cooling for its properties, a higher manganese content is considered desirable to impart sufficient hardenability to achieve a pearlitic microstructure with fine interlamellar spacing. A manganese content of less than 1.1 %Mn was found to be insufficient to achieve the desired hardenability at the chosen carbon content while at levels above 1.4%, the increased risk of formation of martensite, particularly in areas of segregation of manganese, was considered unacceptable.
- a higher level of manganese is also considered undesirable from a welding perspective because of the increased risk of formation of hard and embrittling martensite.
- the manganese content is at most 1.35%.
- a suitable minimum value for the manganese would be 1.20% or even 1.25%.
- vanadium as a precipitation strengthening alloying element has been utilised in this invention to strengthen the pearlitic ferrite and thereby increase the resistance to ratchetting, wear, and rolling contact fatigue.
- Vanadium forms vanadium carbides or vanadium nitrides depending on the amount of nitrogen present in the steel and the temperature. Therefore, it is necessary to examine the level of vanadium addition together with the magnitude of nitrogen in the steel as the efficacy of precipitation strengthening in eutectoid pearlitic steels decreases with increasing levels of nitrogen, which leads to coarser precipitates of vanadium nitride at higher temperatures.
- minimum nitrogen content of 0.003% is considered a practical lower limit while a higher limit of 0.007% is considered desirable to ensure best returns from the additions of costly vanadium.
- higher nitrogen contents could be tolerated provided they are accompanied by proportionately higher vanadium contents.
- the minimum amount of nitrogen is 0.003% coupled with minimum vanadium content of 0.07%.
- nitrogen is at most 0.007% while the corresponding figures for vanadium are 0.07% minimum and 0.12% maximum. Although these maximum contents could be exceeded, they are non-ideal and economically unattractive.
- the wear resistance obtained with the steel according to the invention in the as-rolled condition, accelerated cooling condition or heat treated condition is such that this will reduce the need for the application of a preventive high cost hard facing for rails to be laid in tight curves.
- the phosphorus content of the steel is at most 0.015%.
- Suphur values must be between 0.008 and 0.030% because it forms MnS inclusions. These inclusions act as sinks for any residual hydrogen that may be present in the steel. This hydrogen can result in shatter cracks which can be the initiators of fatigue cracks in the head (also known as tache ovals) under the high stresses from the wheels.
- the addition of at least 0.008% sulphur prevents the deleterious effects of hydrogen, whereas a maximum value of 0.03% is chosen to avoid embrittlement of the structure.
- the maximum value is 0.025%.
- Boron although not a mandatory alloying element, could be used to improve the properties of the steel according to the invention and amounts up to about 60 ppm could be used. Boron is a strong promoter of the formation of microstructural components such as bainite or martensite, particularly when the nitrogen in the steel is bound by titanium. If not, BN-precipitates may be formed. In the steel according to the invention it is important that the microstructure is substantially pearlitic and preferably fully pearlitic and that the amount of bainitic or martensitic microstructural components is kept as low as possible and preferably are absent. Preferably there is no boron in the steel according to the invention as an alloying elements, but it may be present as an inevitable impurity. A boron content of below 0.0005% (i.e. ⁇ 5ppm) is generally considered ineffective as an alloying element and is therefore considered as an impurity in the context of this application.
- the maximum recommended level of unavoidable impurities are based on EN13674-I:2003, according to which the maximum limits are Mo 0.02%, Ni 0.10%, Sn - 0.03%, Sb - 0.020%, Ti - 0.025%, Nb - 0.01%.
- the wear resistance of the steel from the current invention has been established employing the proven comparative "Twin Disk” testing procedure.
- the test is undertaken using a laboratory twin-disc facility similar to the facility described in 'Wear', 162-164 (1993 ), Microstructure and wear resistance of pearlitic rail steels, Albert J. Perez-Unzueta & John H. Beynon 5 . This equipment simulates the forces arising when the wheel is rolling and sliding on the rail.
- These assessments are not part of the formal rail qualification procedure but have been found to provide a good indicator as to the relative in-service performance of different rail steel compositions.
- test conditions for wear testing involve the use of a 560 MPa contact stress and 25% slip while those for RCF utilise a higher contact stress of 900 MPa, 5% slip and water lubrication.
- the results are shown in Figure 1 where the wear rate in mg/m slip is plotted against the hardness (in HV).
- Silicon is a solid solution strengthener and increases the strength of the pearlitic ferrite, thereby increasing the resistance of the pearlite to both wear and RCF initiation.
- the precipitation of fine vanadium carbides within the pearlitic ferrite increases its strength, in particular the proof strength, and thereby the resistance to both wear and RCF.
- a further feature of the compositional design is to limit the nitrogen content in order to prevent the premature formation of relatively coarse precipitates of vanadium nitride, as they are significantly less effective in increasing the strength of the pearlitic ferrite. This ensures that the vanadium additions remain in solution within the austenite to lower temperatures and, therefore, result in finer precipitates.
- a proportion of the vanadium also remains in solution, thereby acting as a hardenability agent to refine the pearlite spacing.
- the specific design of the composition claimed in this embodiment utilises the various attributes of the individual elements to produce a microstructure with a highly desirable combination of wear and RCF resistance.
- the mechanical properties and the resistance to both wear and RCF initiation of the steels in accordance with the invention are better than most conventional heat treated pearlitic rail grades and similar to the hardest heat treated grade (Grade R340GHT) included in the Euro norm for grooved rails (EN 14811:2006 + A1: 2009).
- the proprietary Tata Steel weld restoration process specifies low preheat temperatures of about 60°C to 80°C.
- the fundamental principle on which this process is based is the avoidance of the completion of transformation to martensite within the heat affected zone created by the deposited weld bead.
- the design of the steel composition has had two challenging objectives: firstly to meet the property requirements described in preceding paragraphs and secondly to ensure the martensite start (M s ) and martensite finish (M f ) transformation temperatures are such that they do not permit the transformation to martensite to go to completion during the weld restoration process.
- the M f temperature needs to be below about 60°C and preferably much below this temperature to maximise the volume of untransformed retained austenite that is key to the prevention of the formation of incipient cracks at the weld-parent metal interface or within the heat affected zone formed by the deposition of the weld bead.
- the M f temperature is considered to be about 150°C below the M s temperature which can be calculated using the equations (1), (1a), (1b) and (2) as given above.
- the M s and M f temperature of a range of rail steels available is shown in Figure 2 against the required minimum hardness of the grade.
- the temperatures are the average of those calculated by the two equations given in paragraph 0012 and the concentrations of carbon and manganese used in the calculations are the midpoint values of the range specified in EN 14811:2006 +A1: 2009.
- the M s temperature is the upper value
- the M f temperature is the lower value of the depicted range.
- the steel of this invention referenced as "Invention" in figure 2 , has the lowest M f temperature and hence is capable of retaining the maximum proportion of austenite and therefore most resistant to the formation of incipient cracks.
- the other grooved rail steel grades have undesirably higher M f temperatures implying completion of martensite transformation during weld restoration and a much higher risk of the formation of cracks.
- the excellent wear resistance of the rail ensures that it takes a long time before the rail is worn down in a vertical direction.
- the weld restorability and the fact that the steel according to the invention does not require a heat treatment to achieve its properties ensures that the rail can be repaired in situ, so the rail does not have to be taken out of the street but can be repaired overnight. This involves less road works and less inconvenience for inner city traffic.
- This combination of properties achievable by engineering the microstructure and the chemistry of the rail means that the rail is not only cost effective, but also provides a more ecological solution because rails can be easily repaired and do not have to be replaced by new rails as often.
- careful compositional design thereby eliminating the need for a heat treatment step during rail manufacture, also ensures a greener rail product in comparison with steels which derive their properties from a heat treatment after rolling the rail.
- the steel according to the invention is suitable for purposes such as crane rails or flat-bottomed rails, it has been found that the rail steel is exceptionally suitable for the production of grooved rails that benefit from the combined key attributes of wear resistance and weld restorability.
- a 300 t commercial BOS cast (steel B) was produced of the inventive steel based on the chemistry of lab cast A, and subsequently continuously cast to a 355 x 305 mm bloom section.
- the blooms were rolled to various rail sections and were allowed to cool on the rail cooling bank under the standard cooling conditions as for conventional as-rolled commercial rail grades. All rail lengths were produced free from any internal or surface breaking defects. The rails were tested in the as-hot-rolled condition.
- the chemical compositions of steels A and B are given in Table 1.
- the comparative examples C1-C4 are also given in table 1.
- Table 1 Chemical composition, wt% Steel C Si Mn P S Cr V Al N A 0.76 0.76 1.23 0.016 0.012 0.04 0.08 ⁇ 0.005 49 B 0.76 0.75 1.22 0.018 0.013 0.03 0.09 ⁇ 0.005 32 C1 0.61 0.82 1.40 0.018 0.014 0.62 ⁇ 0.01 0.010 70 C2 0.72 0.83 0.95 0.016 0.011 ⁇ 0.01 0.13 0.008 40 C3 0.65 0.72 1.25 0.015 0.013 ⁇ 0.005 0.13 0.012 60 C4 0.44 0.70 1.21 0.015 0.010 ⁇ 0.005 0.12 0.014 60
- the hardness of the steels A and B was found to be between 330 and 335 HV30.
- the inventors found that by selecting a steel in the narrow chemistry window in accordance with the invention that both wear resistance and RCF resistance are excellent and match the performance of a heat treated Grade 350HT whilst showing similar mechanical properties. In comparison to some grades our inventive steels do not require heat treatment to obtain the desired properties.
- Table 2 Hardness & tensile property data for the inventive steels and current pearlitic rail grades (R260 and R350HT).
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Heat Treatment Of Steel (AREA)
- Heat Treatment Of Articles (AREA)
Description
- This invention relates to a rail steel, particularly for use as a grooved rail such as those used for tramway track, having an excellent combination of properties, in particular, the resistance to both wear and rolling contact fatigue and at the same time being capable of being weld restored without the need for high temperature preheat.
- Cost effectiveness of rail transport has become a significant issue in recent years. Replacing an embedded rail in a tramway network causes service disruptions; not only for the rail traffic, but also for other users of the shared infrastructure as such networks are installed in city centres. Tramway networks are often characterised by very tight track radii that inevitably experience high rates of side wear and hence can be the factor dictating rail life. Thus a key first requirement of a cost effective rail steel grade for tramway applications is its ability to be weld restored without the need for high temperature preheat that damages the surrounding polymer in which the rail is embedded. However, even with this attribute, the factor determining the life of the rail is the rate of vertical head wear and hence the second key requirement of a cost effective rail steel grade is its wear resistance. Moreover, increasing passenger numbers mean that rail traffic has become more intense over the years, causing more wear of the rails. Further improvements in rail material properties are required to make them more tolerant and resistant to the damage resulting from the increased stresses and stress cycles imposed. Although developments in rail metallurgy and heat treatment technology have refined the pearlitic microstructure to increase wear resistance, the need for greater reductions in life cycle costs continues to drive further improvements in the metallurgy of rails.
- Another rail degradation mechanism often encountered on tramway and metro networks is railhead corrugation. Although the development of corrugation is influenced by a variety of system characteristics, it is widely acknowledged that an increase in hardness and yield strength of rail steels slows down the development and growth of corrugation. Consequently a third requirement of cost effective rail steel for tramways and metro networks is an increase in hardness and yield strength.
-
US2009/0134647 refers to a railroad wheel steel with a pearlitic structure, and contains (in weight%) carbon (0.65-0.80), silicon (0.90-1.10), manganese (0.85-1.15), phosphorus (0.001-0.030), niobium (0.009-0.013), sulfur (0.005-0.040) and remainder of iron and unavoidable impurities. The steel further contains chromium (0.10-0.25), nickel (0.050-0.150), molybdenum (0.20-0.30) and vanadium (0.10-0.30). - In straight and gently curved parts of railroads where the experienced rates of wear are generally lower, rail life and associated maintenance costs are also dictated by the need to control the initiation and growth of Rolling Contact Fatigue (RCF) cracks whose origins are either at, or very close to, the rail head surface. RCF can occur in various forms but are commonly referred to as Head Checks (HC), Gauge Corner Cracking (GCC), or as Squat defects. Hence, a fourth requirement of cost effective rail steel for tramways and metro networks is its resistance to the initiation of Rolling Contact Fatigue (RCF).
- Optimisation of wheel and rail profiles to minimise the damaging stresses and the use of regular grinding to maintain the desired profiles while, at the same time, removing the remaining damaged surface layers has become the proven method of control for RCF and corrugation affected track. However, the cost of rail grinding is high and it consumes the time available for running scheduled services. Hence the driver for the development of a more cost effective metallurgical solution remains.
- In addition to the improved resistance to wear, RCF, and corrugation, a further requirement for the design of a novel rail steel is the ability to be repeatedly weld restored in-situ as a mitigation measure to the high rates of side wear experienced in tight curves of tramway networks. The low preheat weld restoration technology, as laid down in Tata Steel patent
GB2443494 - Therefore it is an object of this invention to provide high-strength rails that are highly resistant to wear, rolling contact fatigue, and corrugation while retaining the ability to be repeatedly weld restored.
- It is also an object to provide high-strength rails in which side wear can be easily and robustly restored in-situ by means of a weld deposition treatment.
- It is also an object to provide high-strength rails with a hardness of at least 330 HV, a tensile strength of at least 1000 MPa and yield strength of at least 600MPa.
- One or more of the objects of the invention was achieved with a high-strength pearlitic rail steel having an excellent combination of wear properties, rolling contact fatigue resistance and weld restorability, containing (in weight %):
- 0.70% to 0.85% carbon,
- 0.65% to 1.00% silicon,
- 1.1% to 1.4% manganese,
- 0.07% to 0.15% vanadium,
- up to 0.008% nitrogen,
- up to 0.025% phosphorus,
- 0.008 to 0.030% sulphur,
- at most 2.5 ppm hydrogen,
- at most 0.10% chromium,
- at most 0.010% aluminium,
- at most 20 ppm oxygen,
- the remainder consisting of iron and unavoidable impurities.
- The efficacy of the chemical composition of steels according to the invention is best demonstrated through an explanation of the reasons for the addition of various elements and comparison of the key properties for grooved rail steels.
- Carbon is the most cost effective strengthening alloying element in rail steels as it provides the most cost effective addition to achieve the hardness and strength in fully pearlitic steels. In an embodiment the maximum value of carbon is 0.8%. This reduces the risk of formation of a cementite network at the grain boundaries. More preferably the range of carbon content is from 0.735% to 0.785%. This range provides the optimal balance between the volume fraction of hard cementite and the prevention of the formation of a deleterious network of embrittling cementite at grain boundaries. Carbon is also a potent hardenability agent that facilitates a lower transformation temperature and hence finer interlamellar spacing. The high volume fraction of hard cementite and fine interlamellar spacing provides the wear resistance and contributes towards the increased RCF resistance of the composition included in an embodiment of the invention. Furthermore, as demonstrated by the Tata Steel low preheat weld restoration process1, it is essential to lower the Martensite Start (Ms) temperature of the steel to ensure a robust weld deposit. The prescribed range of carbon is essential to achieve this objective. The following widely accepted methodologies for the calculation of Ms temperature, clearly identify the efficacy of carbon in reducing the magnitude of this parameter. In effect, carbon is between 13 to 17 times more potent in reducing the Ms temperature compared to manganese. According to Andrews (J. Iron & Steel Inst., 183 (1965), pp. 721-727) the Ms Temperature in °C is given by 539 - 423 x % Carbon - 30.4 x % Mn (eq. 1'a) and according to Steven and Haynes (J. Iron & Steel Inst., 183 (1956), pp. 349-359) by 561 - 474 x % Carbon - 33 x % Mn (eq. 1 b). Both regression equations provide slightly different values for Ms. In the context of this invention the average value of these two equations was used as a the approximation of the actual Ms. Mf is then determined from Ms by subtracting 150°C from Ms.


- It is preferable that the Martensite Start (Ms) temperature of the steel is below about 160°Cto ensure a robust weld deposit.
- In this invention the addition of Silicon is an integral and essential part of the design of the steel to engineer the resulting microstructure and properties and not, as in most other rail steels, a reflection of the manufacturing process route rather than an intentional alloying addition. Silicon is often used as a deoxidising element and as such the addition of silicon is usually intended for that purpose only. As the invention refers to a broadly eutectoid composition, the microstructure contains little or no proeutectoid ferrite. Instead it is primarily the interlamellar spacing of the pearlite that dictates the resulting properties. Traditionally, the refinement of the pearlitic microstructure in grooved rail compositions has been achieved trough the use of accelerated cooling. The novelty of the approach in this invention is to treat the pearlitic microstructure as a three-dimensional entity in which the behaviour at the wheel-rail interface is governed by the properties of the two components of pearlite, ferrite and cementite laths, rather than just the bulk properties of hardness and tensile strength. Consequently, the novelty in this invention lies in the use of silicon to strengthen the pearlitic ferrite through solid solution strengthening which in turn imparts an increased resistance to ratchetting, wear, and rolling contact fatigue. A minimum Silicon content of 0.65% is essential for the steel according to the invention to attain the required mechanical property values, wear resistance and RCF resistance. Although Silicon additions have a very limited effect on hardenability of steel and this is reflected in the equations for the calculation of Ms temperature, the addition of up to 1.0% Silicon is acknowledged to make a small contribution to the lowering of the Ms temperature. Silicon content between 0.65% and 0.80% was found to provide a good balance of the required mechanical properties without any adverse effect on weld restorability.
- Manganese is a key alloying element in all grooved rail steels to provide the required hardenability to ensure a relatively fine interlamellar spacing following natural or accelerated cooling of such steels. This purpose remains valid for the current invention. In the current invention, which does not rely on accelerated cooling for its properties, a higher manganese content is considered desirable to impart sufficient hardenability to achieve a pearlitic microstructure with fine interlamellar spacing. A manganese content of less than 1.1 %Mn was found to be insufficient to achieve the desired hardenability at the chosen carbon content while at levels above 1.4%, the increased risk of formation of martensite, particularly in areas of segregation of manganese, was considered unacceptable. A higher level of manganese is also considered undesirable from a welding perspective because of the increased risk of formation of hard and embrittling martensite. In a preferable embodiment, the manganese content is at most 1.35%. A suitable minimum value for the manganese would be 1.20% or even 1.25%.
- The efficacy of vanadium as a precipitation strengthening alloying element has been utilised in this invention to strengthen the pearlitic ferrite and thereby increase the resistance to ratchetting, wear, and rolling contact fatigue. Vanadium forms vanadium carbides or vanadium nitrides depending on the amount of nitrogen present in the steel and the temperature. Therefore, it is necessary to examine the level of vanadium addition together with the magnitude of nitrogen in the steel as the efficacy of precipitation strengthening in eutectoid pearlitic steels decreases with increasing levels of nitrogen, which leads to coarser precipitates of vanadium nitride at higher temperatures. Furthermore, such high temperature precipitates do not strengthen the pearlitic ferrite nor do they leave sufficient vanadium in solution to impart increased hardenability to achieve a finer interlamellar spacing. The additions of vanadium to eutectoid steels do not appreciably affect the Ms temperature. The inventors found that the proportion of vanadium precipitated as carbides was near maximum when the nitrogen content was restricted to 0.003% and this decreased proportionately with increasing nitrogen content. The knowledge of these metallurgical principles has been applied in an innovative manner to arrive at the ideal contents of 0.08% V with 0.003% Nitrogen. Hence, for reasons of cost effective manufacturability, minimum nitrogen content of 0.003% is considered a practical lower limit while a higher limit of 0.007% is considered desirable to ensure best returns from the additions of costly vanadium. However, although not desirable from the point of view of cost effectiveness, higher nitrogen contents could be tolerated provided they are accompanied by proportionately higher vanadium contents.
- In an embodiment of the invention, the minimum amount of nitrogen is 0.003% coupled with minimum vanadium content of 0.07%. Preferably nitrogen is at most 0.007% while the corresponding figures for vanadium are 0.07% minimum and 0.12% maximum. Although these maximum contents could be exceeded, they are non-ideal and economically unattractive.
- Because of the tailored additions of silicon, manganese and vanadium the aimed properties are achieved not only near the surface but also in the head bulk, with a high consistency. This consistency is difficult to achieve in a heat treated rail whereas in the steel according to the invention this consistency is achieved in the as-hot rolled rail. Higher strengths and/or yield strength and/or hardness can be achieved from this steel by subjecting it to accelerated cooling in an in-line or off-line heat treatment facility employing forced air, water, air mist, or polymer quenchants.
- The wear resistance obtained with the steel according to the invention in the as-rolled condition, accelerated cooling condition or heat treated condition is such that this will reduce the need for the application of a preventive high cost hard facing for rails to be laid in tight curves.
- Preferably, the phosphorus content of the steel is at most 0.015%. Suphur values must be between 0.008 and 0.030% because it forms MnS inclusions. These inclusions act as sinks for any residual hydrogen that may be present in the steel. This hydrogen can result in shatter cracks which can be the initiators of fatigue cracks in the head (also known as tache ovals) under the high stresses from the wheels. The addition of at least 0.008% sulphur prevents the deleterious effects of hydrogen, whereas a maximum value of 0.03% is chosen to avoid embrittlement of the structure. Preferably the maximum value is 0.025%. Boron, although not a mandatory alloying element, could be used to improve the properties of the steel according to the invention and amounts up to about 60 ppm could be used. Boron is a strong promoter of the formation of microstructural components such as bainite or martensite, particularly when the nitrogen in the steel is bound by titanium. If not, BN-precipitates may be formed. In the steel according to the invention it is important that the microstructure is substantially pearlitic and preferably fully pearlitic and that the amount of bainitic or martensitic microstructural components is kept as low as possible and preferably are absent. Preferably there is no boron in the steel according to the invention as an alloying elements, but it may be present as an inevitable impurity. A boron content of below 0.0005% (i.e. < 5ppm) is generally considered ineffective as an alloying element and is therefore considered as an impurity in the context of this application.
- The maximum recommended level of unavoidable impurities are based on EN13674-I:2003, according to which the maximum limits are Mo 0.02%, Ni 0.10%, Sn - 0.03%, Sb - 0.020%, Ti - 0.025%, Nb - 0.01%.
- The wear resistance of the steel from the current invention has been established employing the proven comparative "Twin Disk" testing procedure. The test is undertaken using a laboratory twin-disc facility similar to the facility described in 'Wear', 162-164 (1993), Microstructure and wear resistance of pearlitic rail steels, Albert J. Perez-Unzueta & John H. Beynon5. This equipment simulates the forces arising when the wheel is rolling and sliding on the rail. These assessments are not part of the formal rail qualification procedure but have been found to provide a good indicator as to the relative in-service performance of different rail steel compositions. The test conditions for wear testing involve the use of a 560 MPa contact stress and 25% slip while those for RCF utilise a higher contact stress of 900 MPa, 5% slip and water lubrication. The results are shown in
Figure 1 where the wear rate in mg/m slip is plotted against the hardness (in HV). - It is apparent that wear rate decreases as a function of hardness and that beyond a hardness level of 330 Hv30 (~313HB), there is little or no measurable further reduction in the rate of wear. Consequently, one of the objects of the invention was to achieve the wear resistance equivalent to hardness level of at least 330 HV30. The optimised compositions of the invention in both the laboratory and commercial casts have achieved the desired wear resistance. The inventors have found that the balanced chemical composition produces very wear resistant pearlite as a result of the strengthening of the pearlitic ferrite through solid solution strengthening by silicon additions and very finely dispersed vanadium carbides within the pearlitic ferrite laths. Furthermore, by restricting the nitrogen to < 0.007%, the inventors have managed to capitalise on the well known potent hardenability effect of vanadium in solution which enhances the strength, hardness, and wear resistance of the optimised composition of the invention by refining the interlamellar spacing of the pearlite.
- Although, the lower operational speed of tramways in embedded track makes them less susceptible to Rolling Contact Fatigue (RCF), the strengthening of the pearlitic ferrite resulting from the composition of the invention has also improved the resistance of the steel to RCF. An improvement of at least 20% in the resistance to RCF-initiation has been established through comparative laboratory twin disk testing of the composition of the invention and the standard R260 grade.
- A number of factors come together to bring about these improvements. Firstly, increasing the carbon content with respect to the typical lower carbon rail steel grades for grooved rails whilst remaining within the hypo-eutectoid region of the iron-carbon phase diagram, increases the volume fraction of hard cementite in the microstructure. As the carbon content does not encroach into the hyper-eutectoid range of compositions, the risk of forming deleterious networks of embrittling cementite at grain boundaries under the relatively slow cooling experienced by rails during production is avoided. As an additional precautionary measure, the intentional additions of higher silicon and vanadium to the composition have been designed to prevent grain boundary cementite within the segregated portions of the rail section. These additions also have a second, and equally important, function. Silicon is a solid solution strengthener and increases the strength of the pearlitic ferrite, thereby increasing the resistance of the pearlite to both wear and RCF initiation. Similarly, the precipitation of fine vanadium carbides within the pearlitic ferrite increases its strength, in particular the proof strength, and thereby the resistance to both wear and RCF. A further feature of the compositional design is to limit the nitrogen content in order to prevent the premature formation of relatively coarse precipitates of vanadium nitride, as they are significantly less effective in increasing the strength of the pearlitic ferrite. This ensures that the vanadium additions remain in solution within the austenite to lower temperatures and, therefore, result in finer precipitates. A proportion of the vanadium also remains in solution, thereby acting as a hardenability agent to refine the pearlite spacing. Thus the specific design of the composition claimed in this embodiment utilises the various attributes of the individual elements to produce a microstructure with a highly desirable combination of wear and RCF resistance. The mechanical properties and the resistance to both wear and RCF initiation of the steels in accordance with the invention are better than most conventional heat treated pearlitic rail grades and similar to the hardest heat treated grade (Grade R340GHT) included in the Euro norm for grooved rails (EN 14811:2006 + A1: 2009). Although not essential for the current intended application of grooved rails for embedded street running track, further improvements to tensile properties and resistance to wear, plastic deformation, and RCF could be obtained by subjecting the compositions of the invention to accelerated cooling after hot rolling or follow up heat treatment employing a reheating stage.
- Another and equally significant additional attribute of the steels in accordance with the invention is their ability to be weld restored without the need for high temperature preheat. The proprietary Tata Steel weld restoration process specifies low preheat temperatures of about 60°C to 80°C. The fundamental principle on which this process is based is the avoidance of the completion of transformation to martensite within the heat affected zone created by the deposited weld bead. Thus, in this invention, the design of the steel composition has had two challenging objectives: firstly to meet the property requirements described in preceding paragraphs and secondly to ensure the martensite start (Ms) and martensite finish (Mf) transformation temperatures are such that they do not permit the transformation to martensite to go to completion during the weld restoration process. Consequently, the Mf temperature, needs to be below about 60°C and preferably much below this temperature to maximise the volume of untransformed retained austenite that is key to the prevention of the formation of incipient cracks at the weld-parent metal interface or within the heat affected zone formed by the deposition of the weld bead. In general, the Mf temperature is considered to be about 150°C below the Ms temperature which can be calculated using the equations (1), (1a), (1b) and (2) as given above. The Ms and Mf temperature of a range of rail steels available is shown in
Figure 2 against the required minimum hardness of the grade. The temperatures are the average of those calculated by the two equations given in paragraph 0012 and the concentrations of carbon and manganese used in the calculations are the midpoint values of the range specified in EN 14811:2006 +A1: 2009. The Ms temperature is the upper value, the Mf temperature is the lower value of the depicted range. - It is apparent that the steel of this invention, referenced as "Invention" in
figure 2 , has the lowest Mf temperature and hence is capable of retaining the maximum proportion of austenite and therefore most resistant to the formation of incipient cracks. In contrast, the other grooved rail steel grades have undesirably higher Mf temperatures implying completion of martensite transformation during weld restoration and a much higher risk of the formation of cracks. - The excellent wear resistance of the rail ensures that it takes a long time before the rail is worn down in a vertical direction. The weld restorability and the fact that the steel according to the invention does not require a heat treatment to achieve its properties ensures that the rail can be repaired in situ, so the rail does not have to be taken out of the street but can be repaired overnight. This involves less road works and less inconvenience for inner city traffic. This combination of properties achievable by engineering the microstructure and the chemistry of the rail means that the rail is not only cost effective, but also provides a more ecological solution because rails can be easily repaired and do not have to be replaced by new rails as often. Moreover, careful compositional design, thereby eliminating the need for a heat treatment step during rail manufacture, also ensures a greener rail product in comparison with steels which derive their properties from a heat treatment after rolling the rail.
- Although the steel according to the invention is suitable for purposes such as crane rails or flat-bottomed rails, it has been found that the rail steel is exceptionally suitable for the production of grooved rails that benefit from the combined key attributes of wear resistance and weld restorability.
- Laboratory casts of steels C1-C4 and of the inventive steel A were produced as 60 kg ingots. Casts C1 to C4 are preliminary casts that were made to establish the balance amongst the sometimes conflicting requirements of achieving the required hardness, tensile properties, and the resulting wear resistance on one hand with the requirements of a low enough Ms temperature to ensure weld restorability using the low preheat process. The results from these investigations culminated firstly into a laboratory cast of the composition of cast A. The ingots were rolled to 30 mm thick plate and subjected to natural air cooling to accurately simulate the cooling conditions in the head of an as-rolled rail. A 300 t commercial BOS cast (steel B) was produced of the inventive steel based on the chemistry of lab cast A, and subsequently continuously cast to a 355 x 305 mm bloom section. The blooms were rolled to various rail sections and were allowed to cool on the rail cooling bank under the standard cooling conditions as for conventional as-rolled commercial rail grades. All rail lengths were produced free from any internal or surface breaking defects. The rails were tested in the as-hot-rolled condition.
- The chemical compositions of steels A and B are given in Table 1. The comparative examples C1-C4 are also given in table 1.
Table 1: Chemical composition, wt% Steel C Si Mn P S Cr V Al N A 0.76 0.76 1.23 0.016 0.012 0.04 0.08 < 0.005 49 B 0.76 0.75 1.22 0.018 0.013 0.03 0.09 < 0.005 32 C1 0.61 0.82 1.40 0.018 0.014 0.62 < 0.01 0.010 70 C2 0.72 0.83 0.95 0.016 0.011 <0.01 0.13 0.008 40 C3 0.65 0.72 1.25 0.015 0.013 <0.005 0.13 0.012 60 C4 0.44 0.70 1.21 0.015 0.010 <0.005 0.12 0.014 60 - The hardness of the steels A and B was found to be between 330 and 335 HV30. The inventors found that by selecting a steel in the narrow chemistry window in accordance with the invention that both wear resistance and RCF resistance are excellent and match the performance of a heat treated Grade 350HT whilst showing similar mechanical properties. In comparison to some grades our inventive steels do not require heat treatment to obtain the desired properties.
Table 2: Hardness & tensile property data for the inventive steels and current pearlitic rail grades (R260 and R350HT). Steel Condition 0.2% PS (MPa) TS (MPa) EI (%) Hardness (HV30) R260 As-rolled 494 907 12.5 290 R350HT Heat treated 763 1210 14.0 375 A As-rolled 646 1089 10.0 331 B As-rolled 629 1100 9.8 335
Claims (10)
- Steel for the manufacture of rails, particularly of grooved rails, having a hardness of at least 330 HV30, a tensile strength of at least 1000 MPa and a yield strength of at least 600 MPa consisting of in weight %,• 0.70% to 0.85 carbon,• 0.65% to 1.00% silicon,• 1.1% to 1.4% manganese,• 0.07% to 0.15% vanadium,• up to 0.008% nitrogen,• up to 0.025% phosphorus,• 0.008 to 0.030% sulphur,• at most 2.5 ppm hydrogen,• at most 0.10% chromium,• at most 0.010% aluminium,• at most 20 ppm oxygen,• the remainder consisting of iron and unavoidable impurities.
- Steel according to claim 1 wherein the martensite start transformation temperature (Ms) as determined by eq. 1 is below 190°C and wherein martensite finish transformation (Mf) according to eq. 2 is below 40°C.

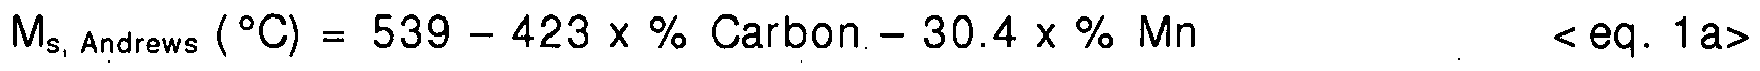


- Steel according to claim 1 comprising a carbon content of at least 0.735%C, preferably of at least 0.75%.
- Steel according to claim 1 or 2 comprising a manganese content of at least 1.20%.
- Steel according to any one of claims 1 to 3 comprising a silicon content of at least 0.75%.
- Steel according to any one of claims 1 to 5 comprising a combination of a vanadium content of at least 0.08% V and a nitrogen content of at most 0.005%.
- Steel according to any one of claims 1 to 5 comprising a combination of a vanadium content of at least 0.10% V and a nitrogen content of at most 0.007%.
- Steel according to any one of claims 1 to 7 wherein the martensite start transformation temperature as determined by eq. 1 is below 175°C and wherein martensite finish transformation according to eq. 2 is bellow 25°C.
- Steel according to any one of claims 1 to 8 wherein heat affected zone of the weld restoration bead comprises at least 50% in volume of retained austenite.
- Rail, such as grooved rail, crane rail or flat bottomed rail, made from the steel according to any one of claims 1 to 9 having a hardness of at least 330 HV, a tensile strength of at least 1000 MPa and a yield strength of at least 600 MPa.
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP12791480.2A EP2785890B1 (en) | 2011-11-28 | 2012-11-26 | Rail steel with an excellent combination of wear properties, rolling contact fatigue resistance and weldability |
| PL12791480T PL2785890T3 (en) | 2011-11-28 | 2012-11-26 | Rail steel with an excellent combination of wear properties, rolling contact fatigue resistance and weldability |
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP11190973 | 2011-11-28 | ||
| EP12791480.2A EP2785890B1 (en) | 2011-11-28 | 2012-11-26 | Rail steel with an excellent combination of wear properties, rolling contact fatigue resistance and weldability |
| PCT/EP2012/073606 WO2013079438A1 (en) | 2011-11-28 | 2012-11-26 | Rail steel with an excellent combination of wear properties, rolling contact fatigue resistance and weldability |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2785890A1 EP2785890A1 (en) | 2014-10-08 |
| EP2785890B1 true EP2785890B1 (en) | 2015-07-15 |
Family
ID=47227803
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12791480.2A Active EP2785890B1 (en) | 2011-11-28 | 2012-11-26 | Rail steel with an excellent combination of wear properties, rolling contact fatigue resistance and weldability |
Country Status (10)
| Country | Link |
|---|---|
| EP (1) | EP2785890B1 (en) |
| JP (1) | JP6270730B2 (en) |
| BR (1) | BR112014012660B1 (en) |
| DK (1) | DK2785890T3 (en) |
| ES (1) | ES2545659T3 (en) |
| HU (1) | HUE027275T2 (en) |
| MA (1) | MA35745B1 (en) |
| PL (1) | PL2785890T3 (en) |
| PT (1) | PT2785890E (en) |
| WO (1) | WO2013079438A1 (en) |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104195433B (en) * | 2014-09-02 | 2016-08-31 | 攀钢集团攀枝花钢铁研究院有限公司 | A kind of high-strength tenacity pearlite steel rail and production method thereof |
| CN105112786B (en) * | 2015-09-29 | 2017-04-12 | 燕山大学 | Super pearlite steel for steel rails and method for preparing super pearlite steel |
| AU2016374421B2 (en) * | 2015-12-15 | 2019-08-01 | Jfe Steel Corporation | Method for selecting rail steel and wheel steel |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0136741A1 (en) | 1983-08-24 | 1985-04-10 | KOLBENSCHMIDT Aktiengesellschaft | Piston for internal-combustion engines |
| JPS6324045A (en) | 1986-07-16 | 1988-02-01 | Nippon Kokan Kk <Nkk> | Wear-resistant, high-performance rail with excellent ability to stop unstable fracture propagation |
| US4767475A (en) | 1985-10-24 | 1988-08-30 | Nippon Kokan Kabushiki Kaisha | Wear resistant rails having capability of preventing propagation of unstable rupture |
| EP0469560A1 (en) | 1990-07-30 | 1992-02-05 | Burlington Northern Railroad Company | High-strength, damage-resistant rail |
| JPH06279928A (en) | 1993-03-29 | 1994-10-04 | Nippon Steel Corp | High-strength rail with excellent toughness and ductility and its manufacturing method |
| JPH06340951A (en) | 1993-03-12 | 1994-12-13 | Nippon Steel Corp | High strength rail excellent in toughness and its production |
| US20020011283A1 (en) | 1996-07-04 | 2002-01-31 | Masahisa Fujikake | High-strength, damage-resistant rail having hardness distribution of excellent damage-resistance at its head top portion |
| GB2443494A (en) | 2006-07-14 | 2008-05-07 | Corus Uk Ltd | A method of weld repairing or cladding a steel bloom , rail or other part of a railway |
| EP2006406A1 (en) | 2006-03-16 | 2008-12-24 | JFE Steel Corporation | High-strength pearlite rail with excellent delayed-fracture resistance |
| WO2009103565A1 (en) | 2008-02-22 | 2009-08-27 | Corus Uk Limited | Rail steel with an excellent combination of wear properties and rolling contact fatigue resistance |
Family Cites Families (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4895605A (en) * | 1988-08-19 | 1990-01-23 | Algoma Steel Corporation | Method for the manufacture of hardened railroad rails |
| DE69629161T2 (en) * | 1995-03-14 | 2004-04-15 | Nippon Steel Corp. | METHOD FOR PRODUCING RAILS WITH HIGH WEAR RESISTANCE AND HIGH RESISTANCE TO INNER DEFECTS |
| JP3516189B2 (en) * | 1996-01-23 | 2004-04-05 | 住友金属工業株式会社 | Wheels for railway vehicles excellent in wear resistance and heat crack resistance and method of manufacturing the same |
| JPH09316598A (en) * | 1996-03-27 | 1997-12-09 | Nippon Steel Corp | Perlite rail with excellent wear resistance and weldability, and method of manufacturing the same |
| JP2000129397A (en) * | 1998-10-30 | 2000-05-09 | Nkk Corp | Pearlitic rail with excellent wear resistance and ductility |
| JP3513427B2 (en) * | 1999-05-31 | 2004-03-31 | 新日本製鐵株式会社 | Pearlitic rail excellent in wear resistance and internal fatigue damage resistance, and method of manufacturing the same |
| US6387191B1 (en) * | 2000-07-21 | 2002-05-14 | Transportation Technology Center, Inc. | Railway wheels resistant to martensite transformation |
| US6783610B2 (en) * | 2001-03-05 | 2004-08-31 | Amsted Industries Incorporated | Railway wheel alloy |
| JP4571759B2 (en) * | 2001-06-01 | 2010-10-27 | 新日本製鐵株式会社 | Perlite rail and manufacturing method thereof |
| JP2005146346A (en) * | 2003-11-14 | 2005-06-09 | Nippon Steel Corp | Method for producing pearlitic rail with excellent toughness and ductility |
| JP5401762B2 (en) * | 2006-03-16 | 2014-01-29 | Jfeスチール株式会社 | High-strength pearlite rail with excellent delayed fracture resistance |
| CN100482812C (en) * | 2006-09-12 | 2009-04-29 | 攀枝花钢铁(集团)公司 | Rail heat processing method and rail heat processing unit |
| US7591909B2 (en) * | 2007-08-23 | 2009-09-22 | Transportation Technology Center, Inc. | Railroad wheel steels having improved resistance to rolling contact fatigue |
| US7559999B2 (en) * | 2007-08-23 | 2009-07-14 | Transportation Technology Center, Inc. | Railroad wheel steels having improved resistance to rolling contact fatigue |
| JP5238930B2 (en) * | 2009-02-12 | 2013-07-17 | Jfeスチール株式会社 | Abrasion resistant rail and method of manufacturing the same |
| US20110189047A1 (en) * | 2010-02-02 | 2011-08-04 | Transportation Technology Center, Inc. | Railroad rail steels resistant to rolling contact fatigue |
-
2012
- 2012-11-26 ES ES12791480.2T patent/ES2545659T3/en active Active
- 2012-11-26 PL PL12791480T patent/PL2785890T3/en unknown
- 2012-11-26 HU HUE12791480A patent/HUE027275T2/en unknown
- 2012-11-26 DK DK12791480.2T patent/DK2785890T3/en active
- 2012-11-26 WO PCT/EP2012/073606 patent/WO2013079438A1/en not_active Ceased
- 2012-11-26 PT PT127914802T patent/PT2785890E/en unknown
- 2012-11-26 BR BR112014012660-7A patent/BR112014012660B1/en not_active IP Right Cessation
- 2012-11-26 EP EP12791480.2A patent/EP2785890B1/en active Active
- 2012-11-26 JP JP2014542876A patent/JP6270730B2/en not_active Expired - Fee Related
-
2014
- 2014-06-25 MA MA37151A patent/MA35745B1/en unknown
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0136741A1 (en) | 1983-08-24 | 1985-04-10 | KOLBENSCHMIDT Aktiengesellschaft | Piston for internal-combustion engines |
| US4767475A (en) | 1985-10-24 | 1988-08-30 | Nippon Kokan Kabushiki Kaisha | Wear resistant rails having capability of preventing propagation of unstable rupture |
| JPS6324045A (en) | 1986-07-16 | 1988-02-01 | Nippon Kokan Kk <Nkk> | Wear-resistant, high-performance rail with excellent ability to stop unstable fracture propagation |
| EP0469560A1 (en) | 1990-07-30 | 1992-02-05 | Burlington Northern Railroad Company | High-strength, damage-resistant rail |
| JPH06340951A (en) | 1993-03-12 | 1994-12-13 | Nippon Steel Corp | High strength rail excellent in toughness and its production |
| JPH06279928A (en) | 1993-03-29 | 1994-10-04 | Nippon Steel Corp | High-strength rail with excellent toughness and ductility and its manufacturing method |
| US20020011283A1 (en) | 1996-07-04 | 2002-01-31 | Masahisa Fujikake | High-strength, damage-resistant rail having hardness distribution of excellent damage-resistance at its head top portion |
| EP2006406A1 (en) | 2006-03-16 | 2008-12-24 | JFE Steel Corporation | High-strength pearlite rail with excellent delayed-fracture resistance |
| GB2443494A (en) | 2006-07-14 | 2008-05-07 | Corus Uk Ltd | A method of weld repairing or cladding a steel bloom , rail or other part of a railway |
| WO2009103565A1 (en) | 2008-02-22 | 2009-08-27 | Corus Uk Limited | Rail steel with an excellent combination of wear properties and rolling contact fatigue resistance |
Non-Patent Citations (1)
| Title |
|---|
| HIROYASU YOKOYAMA ET AL.: "High Strength Bainitic Steel Rails for Heavy Haul Railways with Superior Damage Resistance", NKK TECHNICAL REVIEW, no. 84, July 2001 (2001-07-01), pages 44 - 51, XP055290755 |
Also Published As
| Publication number | Publication date |
|---|---|
| HUE027275T2 (en) | 2016-10-28 |
| JP2015504484A (en) | 2015-02-12 |
| ES2545659T3 (en) | 2015-09-14 |
| MA35745B1 (en) | 2014-12-01 |
| DK2785890T3 (en) | 2015-08-24 |
| PT2785890E (en) | 2015-10-01 |
| JP6270730B2 (en) | 2018-01-31 |
| BR112014012660B1 (en) | 2018-12-04 |
| EP2785890A1 (en) | 2014-10-08 |
| PL2785890T3 (en) | 2015-12-31 |
| WO2013079438A1 (en) | 2013-06-06 |
| BR112014012660A2 (en) | 2017-06-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3719149B1 (en) | High-hardness steel product and method of manufacturing the same | |
| EP2881487B1 (en) | Abrasion resistant steel plate with super-high strength and high toughness, and process for preparing same | |
| RU2476617C1 (en) | Pearlite rails | |
| EP2881486B1 (en) | Abrasion resistant steel plate with high strength and high toughness, and process for preparing same | |
| AU2009216933B2 (en) | Rail steel with an excellent combination of wear properties and rolling contact fatigue resistance | |
| EP3717142B1 (en) | Method for manufacturing a rail and corresponding rail | |
| US20150028165A1 (en) | Steel for producing parts for railway, railway crossings and switches and method for producing said parts | |
| DK2785890T3 (en) | RAIL STEEL WITH A UNIQUE COMBINATION OF WEAR PROPERTIES OF FATIGUE STRENGTH BY ROLLER CONTACT AND weldability | |
| CA3048723C (en) | Track part made of a hypereutectoid steel | |
| KR101353838B1 (en) | Wear resistant steel having excellent toughness and weldability | |
| US6387191B1 (en) | Railway wheels resistant to martensite transformation | |
| US20190226062A1 (en) | Multi-phase steel especially for production of standard-gauge rails | |
| OA20006A (en) | Track Part Made of a Hypereutectoid Steel. | |
| Steele | Chicago, IL 60616 | |
| Ray et al. | Frontiers of micro-alloyed steel for industrial merchandising-1 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20140630 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R079 Ref document number: 602012008838 Country of ref document: DE Free format text: PREVIOUS MAIN CLASS: C22C0038020000 Ipc: C21D0009040000 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C22C 38/02 20060101ALI20150319BHEP Ipc: C21D 9/04 20060101AFI20150319BHEP Ipc: C22C 38/46 20060101ALI20150319BHEP Ipc: C22C 38/12 20060101ALI20150319BHEP Ipc: C22C 38/04 20060101ALI20150319BHEP Ipc: C22C 38/24 20060101ALI20150319BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20150423 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PCOW Free format text: NEW ADDRESS: C/O TATA STEEL NEDERLAND TECHNOLOGY B.V. GROUP INTELLECTUAL PROPERTY SERVICES - 3G.37 PO BOX 10000, 1970 CA IJMUIDEN (NL) |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 736836 Country of ref document: AT Kind code of ref document: T Effective date: 20150815 |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 Effective date: 20150820 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602012008838 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2545659 Country of ref document: ES Kind code of ref document: T3 Effective date: 20150914 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20150818 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: T2 Effective date: 20150715 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: T3 Ref document number: E 19143 Country of ref document: SK |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20151016 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: UEP Ref document number: 736836 Country of ref document: AT Kind code of ref document: T Effective date: 20150715 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R026 Ref document number: 602012008838 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: VOESTALPINE SCHIENEN GMBH Effective date: 20160415 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: BRITISH STEEL LIMITED |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E027275 Country of ref document: HU |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 5 |
|
| PLAF | Information modified related to communication of a notice of opposition and request to file observations + time limit |
Free format text: ORIGINAL CODE: EPIDOSCOBS2 |
|
| PLAS | Information related to reply of patent proprietor to notice(s) of opposition deleted |
Free format text: ORIGINAL CODE: EPIDOSDOBS3 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20161110 AND 20161116 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 602012008838 Country of ref document: DE Owner name: JINGYE STEEL (UK) LTD, GB Free format text: FORMER OWNER: TATA STEEL UK LTD., LONDON, GB Ref country code: DE Ref legal event code: R081 Ref document number: 602012008838 Country of ref document: DE Owner name: BRITISH STEEL LIMITED, SCUNTHORPE, GB Free format text: FORMER OWNER: TATA STEEL UK LTD., LONDON, GB |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PFA Owner name: BRITISH STEEL LIMITED, GB Free format text: FORMER OWNER: LONGS STEEL UK LIMITED, GB Ref country code: CH Ref legal event code: PUE Owner name: LONGS STEEL UK LIMITED, GB Free format text: FORMER OWNER: TATA STEEL UK LIMITED, NL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 Ref country code: IS Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150715 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: PD Owner name: BRITISH STEEL LIMITED; GB Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), ASSIGNMENT; FORMER OWNER NAME: TATA STEEL UK LTD Effective date: 20170726 |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: FH1C Free format text: FORMER REPRESENTATIVE(S): IVANKA GABOR, ARINOVA SZABADALMI ES VEDJEGY IRODA, HU Representative=s name: OPPENHEIM UEGYVEDI IRODA, HU Ref country code: HU Ref legal event code: GB9C Owner name: BRITISH STEEL LIMITED, GB Free format text: FORMER OWNER(S): TATA STEEL UK LTD, GB |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: PC4A Ref document number: E 19143 Country of ref document: SK Owner name: BRITISH STEEL LIMITED, SCUNTHORPE, NORTH LINCO, GB Free format text: FORMER OWNER: TATA STEEL UK LTD, LONDON, GB Effective date: 20171012 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: SWISSBERG AG, CH |
|
| PLCK | Communication despatched that opposition was rejected |
Free format text: ORIGINAL CODE: EPIDOSNREJ1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R100 Ref document number: 602012008838 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| PLBN | Opposition rejected |
Free format text: ORIGINAL CODE: 0009273 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION REJECTED |
|
| 27O | Opposition rejected |
Effective date: 20180504 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150715 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: FP Effective date: 20150820 Ref country code: BE Ref legal event code: HC Owner name: BRITISH STEEL LIMITED; GB Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), CHANGEMENT NOM PROPRIETAIRE, NOM/ADRESSE; FORMER OWNER NAME: LONGS STEEL UK LIMITED Effective date: 20170421 Ref country code: BE Ref legal event code: PD Owner name: LONGS STEEL UK LIMITED; GB Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), AFFECTATION / CESSION; FORMER OWNER NAME: TATA STEEL UK LTD Effective date: 20170421 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20191122 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: ISLER AND PEDRAZZINI AG, CH Ref country code: CH Ref legal event code: PUE Owner name: JINGYE STEEL (UK) LTD, GB Free format text: FORMER OWNER: BRITISH STEEL LIMITED, GB |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20200604 AND 20200610 |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: CHAD Owner name: JINGYE STEEL (UK) LTD, GB Ref country code: NO Ref legal event code: CREP Representative=s name: ONSAGERS AS, POSTBOKS 1813, VIKA, 0123 OSLO, NORGE |
|
| REG | Reference to a national code |
Ref country code: LU Ref legal event code: PD Owner name: JINGYE STEEL (UK) LTD; GB Free format text: FORMER OWNER: BRITISH STEEL LIMITED Effective date: 20200624 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: PC2A Owner name: JINGYE STEEL (UK) LTD Effective date: 20200716 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: PD Owner name: JINGYE STEEL (UK) LTD; GB Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), CESSION; FORMER OWNER NAME: BRITISH STEEL LIMITED Effective date: 20200513 |
|
| REG | Reference to a national code |
Ref country code: FI Ref legal event code: PCE Owner name: JINGYE STEEL (UK) LTD |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: GB9C Owner name: JINGYE STEEL (UK) LTD, GB Free format text: FORMER OWNER(S): TATA STEEL UK LTD, GB; BRITISH STEEL LIMITED, GB |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 602012008838 Country of ref document: DE Ref country code: DE Ref legal event code: R081 Ref document number: 602012008838 Country of ref document: DE Owner name: JINGYE STEEL (UK) LTD, GB Free format text: FORMER OWNER: BRITISH STEEL LIMITED, SCUNTHORPE, NORTH LINCOLNSHIRE, GB |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: PC4A Ref document number: E 19143 Country of ref document: SK Owner name: JINGYE STEEL (UK) LTD, LONDON, GB Free format text: FORMER OWNER: BRITISH STEEL LIMITED, SCUNTHORPE, NORTH LINCOLNSHIRE, GB Effective date: 20200825 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 736836 Country of ref document: AT Kind code of ref document: T Owner name: BRITISH STEEL LIMITED, Effective date: 20201201 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20201222 Year of fee payment: 9 Ref country code: FI Payment date: 20201130 Year of fee payment: 9 Ref country code: IT Payment date: 20201130 Year of fee payment: 9 Ref country code: SE Payment date: 20201130 Year of fee payment: 9 Ref country code: CZ Payment date: 20201204 Year of fee payment: 9 Ref country code: RO Payment date: 20201204 Year of fee payment: 9 Ref country code: PT Payment date: 20201207 Year of fee payment: 9 Ref country code: NO Payment date: 20201202 Year of fee payment: 9 Ref country code: DK Payment date: 20201130 Year of fee payment: 9 Ref country code: IE Payment date: 20201130 Year of fee payment: 9 Ref country code: CH Payment date: 20201221 Year of fee payment: 9 Ref country code: HU Payment date: 20201218 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20201130 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20201130 Year of fee payment: 9 Ref country code: LU Payment date: 20201130 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20210122 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SK Payment date: 20210504 Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: HC Owner name: BRITISH STEEL LIMITED; GB Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), CHANGE OF OWNER(S) NAME; FORMER OWNER NAME: JINGYE STEEL (UK) LTD Effective date: 20210726 Ref country code: NL Ref legal event code: PD Owner name: JINGYE STEEL (UK) LTD; GB Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), ASSIGNMENT; FORMER OWNER NAME: TATA STEEL UK LTD Effective date: 20210726 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 736836 Country of ref document: AT Kind code of ref document: T Owner name: JINGYE STEEL (UK) LTD, GB Effective date: 20210617 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20201214 Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP Effective date: 20211130 |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: MMEP |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: FI Ref legal event code: MAE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20211201 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 736836 Country of ref document: AT Kind code of ref document: T Effective date: 20211126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211127 Ref country code: RO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220526 Ref country code: NO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211130 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 Ref country code: HU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211127 Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211130 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20211130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211130 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211130 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20230224 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211127 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211126 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 602012008838 Country of ref document: DE Owner name: BRITISH STEEL LTD., SCUNTHORPE, GB Free format text: FORMER OWNER: JINGYE STEEL (UK) LTD, LONDON, GB |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251119 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20251121 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20251125 Year of fee payment: 14 |