EP2481497B1 - Verfahren zum Herstellen eines metallischen Bauteils - Google Patents
Verfahren zum Herstellen eines metallischen Bauteils Download PDFInfo
- Publication number
- EP2481497B1 EP2481497B1 EP20110190029 EP11190029A EP2481497B1 EP 2481497 B1 EP2481497 B1 EP 2481497B1 EP 20110190029 EP20110190029 EP 20110190029 EP 11190029 A EP11190029 A EP 11190029A EP 2481497 B1 EP2481497 B1 EP 2481497B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- metal
- nonwoven
- thixotropic
- rollers
- reinforcement
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21H—MAKING PARTICULAR METAL OBJECTS BY ROLLING, e.g. SCREWS, WHEELS, RINGS, BARRELS, BALLS
- B21H8/00—Rolling metal of indefinite length in repetitive shapes specially designed for the manufacture of particular objects, e.g. checkered sheets
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21J—FORGING; HAMMERING; PRESSING METAL; RIVETING; FORGE FURNACES
- B21J5/00—Methods for forging, hammering, or pressing; Special equipment or accessories therefor
- B21J5/004—Thixotropic process, i.e. forging at semi-solid state
Definitions
- the invention relates to a method for producing a metallic component by forming a heated to the thixotropic state, metallic nonwoven fabric, according to the preamble of claim 1 or 2.
- the air inclusions during pressing of the thixotropically heated metal fiber fleece are selectively expelled in the rolling direction of the pressure roller and can escape freely there from the still unpressed and air-permeable nonwoven material, so that a bubble or voids formation is effectively prevented in the finished component , with the further effect that compliance with the narrow thixotropic temperature window is limited to the relatively narrow contact area of the pressure roller and therefore does not have to be distributed homogeneously over the entire component surface at the time of forming, which considerably simplifies the process-dependent tight temperature control.
- even metallic sheet metal strips of any length can be produced in a production-technically simple manner by means of the thixoforming of a metal fiber fleece.
- a significant improvement of the mechanical component properties is achieved in a particularly preferred embodiment of the invention in that a reinforcement is inserted into the metal fiber fleece prior to the Thixoumformung and this is impregnated under the action of the pressure roller (s) with the metallic nonwoven material as a matrix, wherein the pressure roller deformation of the nonwoven fabric contributes significantly to a bubble-free, material or at least positive engagement of the reinforcement in the metal matrix.
- a reinforcement is inserted into the metal fiber fleece prior to the Thixoumformung and this is impregnated under the action of the pressure roller (s) with the metallic nonwoven material as a matrix, wherein the pressure roller deformation of the nonwoven fabric contributes significantly to a bubble-free, material or at least positive engagement of the reinforcement in the metal matrix.
- preferably unidirectional or multidirectional or even quasi-isotropically oriented metallic, but also non-metallic reinforcing fibers are used as reinforcement
- carbon fibers which are temperature resistant with respect to the Thixotemperatur of the nonwoven material.
- the metal fleece is expediently preheated close to the thixo state before the pressure roll contact, and inductive heating of the metal fleece is preferred in view of rapid full volumetric heating.
- the manufacturing quality of the components can be further improved by pre-compacting the metal fleece prior to the thixotropic pressure roll forming and subsequently recalibrating it by means of a pressure feed.
- a nonwoven fabric which, as preferred, contains aluminum as its main component
- a nonwoven fabric which, as preferred, contains aluminum as its main component
- another advantage of the claimed method is shown.
- the oxide layer is at the Thixoumformung an aluminum nonwoven fabric at The compaction of the aluminum fibers broken, so that the microstructure in the finished aluminum part of the oxide formation of the starting material remains largely unaffected.
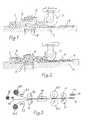
- a metal fiber fleece 1 made of aluminum or an aluminum alloy is placed on a forming bed 2 and locally doubled by an additional non-woven pad 3, so as to produce an aluminum part 4 with a changing wall thickness.
- the fiber web 1 is heated in the contact area of the pressure roller 5 in the thixotropic state and pressed together, on the fiber material, a homogeneous aluminum part 4 is formed, the air inclusions in the fiber web 1 under the effect of Pressure roller 5 are squeezed out in the direction of forward and can escape freely from the still air-permeable nonwoven fabric 1 there.
- the fiber material is preheated in the running direction in front of the pressure roller 5 to near the thixotemperature by means of an induction heater 6 effective between the forming bed 2 and the fleece top side.
- the reinforcement 7 is impregnated with the thixotropic nonwoven material, so that the component 4 has a homogeneous metal structure with an at least positive and a metallic reinforcement in it 7 depending on the fleece and reinforcing material also integrally integrated reinforcement 7, through which the material properties are significantly improved over a pure single-component.
- a plurality of layers consisting of an upper and a lower metallic fiber fleece layer 9.1, 9.2 and an intermediate reinforcement 10, for example a carbon fiber fabric, are respectively drawn from a supply roll 11.1, 11.2 and 12 and between two pre-press rolls 13 merged and precompressed to a denser composite material.
- the precompressed, but still flexible composite material 9, 10 passes through a heating device 14, at which it is preheated to a temperature level even below the thixotropic state of the metal fibers of the fiber fleece layers 9.
- the thus preheated, but still inhomogeneous composite material 9, 10 is then heated in the nip of two pressure rollers 15.1, 15.2 to the thixotropic state and simultaneously the nonwoven layers 9 in this state by the Walzenandruck to an endless metal strip 8 with a homogeneous metal structure 16 and in this matrix-embedded reinforcement 10 is pressed.
- the thixotropic nonwoven fabric material is made to flow uniformly, so that even the finest structures of the reinforcing fibers 10 enclosed by this and thereby cavities are filled. This forms a positive connection and depending on the nature of the reinforcing material also creates a local material connection. Subsequently, a recalibration is still carried out on a roller pair 17 in order to prevent a solidification porosity.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Nonwoven Fabrics (AREA)
Description
- Die Erfindung bezieht sich auf ein Verfahren zum Herstellen eines metallischen Bauteils durch Umformen eines auf den thixotropen Zustand erwärmten, metallischen Faservlieses, nach dem Oberbegriff des Patentanspruchs 1 bzw. 2.
- Es ist bekannt, dass metallische Werkstoffe in einem engen Temperaturintervall kurz unterhalb der Liquidustemperatur in den thixotropen Zustand gelangen und sich dann mit geringem Energieaufwand zu Bauteilen mit hohen mechanischen Kennwerten umformen lassen. Nach dem in der
DE 10 2009 015 418 A1 offenbarten Verfahren der eingangs genannten Art wird als in dieser Hinsicht besonders vorteilhaftes Ausgangsmaterial ein Metallfaservlies verwendet, welches in einem Pressenwerkzeug in den thixotropen Zustand aufgeheizt und zu einem homogen strukturierten Bauteil verpresst wird, wobei sich die mechanischen Eigenschaften noch dadurch deutlich verbessern lassen, dass in das Faservlies eine Armierung eingelegt wird, die dann bei der thixotropen Faservliesumformung im Pressenwerkzeug - anders als bei Verbundbauteilen, die aus einer hochfesten Zwischenschicht und auf diese lediglich aufplattierten Deckschichten bestehen - vollständig mit dem metallischen Vliesmaterial als Matrix durchtränkt wird. Problematisch bei einer solchen thixotropen Faservliesumformung ist jedoch, dass beim Verpressen des Faservlieses Lufteinschlüsse im Thixomaterial verbleiben können, die sich dann im fertigen Bauteil als festigkeits- und steifigkeitsmindernde Lunkerstellen zeigen. Hinzukommt, dass sich die Einstellung einer homogenen Temperaturverteilung bei gleichzeitig engem Temperaturfenster vor allem bei ausgedehnteren Bauteilen äußerst aufwändig und kostenintensiv gestaltet. - Demgegenüber ist es Aufgabe der Erfindung, ein Verfahren der eingangs genannten Art so auszubilden, dass sich durch eine Thixoumformung eines Metallfaservlieses problemlos auch ausgedehntere Bauteile auf baulich und steuerungsmäßig einfache Weise mit hochwertigen mechanischen Eigenschaften herstellen lassen.
- Diese Aufgabe wird erfindungsgemäß durch das im Patentanspruch 1 bzw. 2 gekennzeichnete Herstellungsverfahren gelöst.
- Erfindungsgemäß wird aufgrund der beanspruchten Druckwalzenumformung sichergestellt, dass die Lufteinschlüsse beim Verpressen des thixotrop erwärmten Metallfaservlieses gezielt in Rollrichtung der Druckwalze ausgetrieben werden und aus dem dort noch unverpressten und luftdurchlässigen Faservliesmaterial frei entweichen können, so dass eine Blasen- oder Lunkerbildung im fertigen Bauteil wirksam unterbunden wird, mit dem weiteren Effekt, dass die Einhaltung des engen thixotropen Temperaturfensters auf den relativ schmalen Kontaktbereich der Druckwalze beschränkt ist und daher im Umformzeitpunkt nicht homogen über die gesamte Bauteilfläche verteilt sein muss, wodurch sich die prozessbedingt enge Temperatursteuerung erheblich vereinfacht. Darüberhinaus lassen sich mit der Erfindungsvariante nach Anspruch 2 im Wege der Thixoumformung eines Metallfaservlieses sogar metallische Blechbänder in beliebiger Länge auf fertigungstechnisch einfache Weise herstellen.
- Eine deutliche Verbesserung der mechanischen Bauteileigenschaften wird in besonders bevorzugter Ausgestaltung der Erfindung dadurch erzielt, dass in das Metallfaservlies vor der Thixoumformung eine Armierung eingelegt und diese unter der Einwirkung der Druckwalze(n) mit dem metallischen Faservliesmaterial als Matrix durchtränkt wird, wobei die Druckwalzenumformung des Faservlieses ganz wesentlich zu einer blasenfreien, stoff- oder zumindest formschlüssigen Einbindung der Armierung in die Metallmatrix beiträgt. Als Armierung werden je nach Richtung der für das Bauteil vorgesehenen Betriebslasten vorzugsweise uni- oder multidirektional oder auch quasi-isotrop orientierte metallische, aber auch nicht-metallische Verstärkungsfasern verwendet, und zwar mit besonderem Vorteil Carbonfasern, die bezüglich der Thixotemperatur des Vliesmaterial temperaturbeständig sind.
- Um die Aufheizzeit des Metallfaservlieses im Kontaktbereich der Druckwalze(n) zu verkürzen, wird das Metallvlies vor dem Druckwalzenkontakt zweckmäßigerweise bis nahe an den Thixozustand vorgewärmt, und im Hinblick auf eine rasche vollvolumetrische Aufheizung wird eine induktive Erwärmung des Metallvlieses bevorzugt.
- Die Fertigungsqualität der Bauteile lässt sich dadurch weiter verbessern, dass das Metallvlies vor der thixotropen Druckwalzenumformung vorverdichtet und im Anschluss an diese durch eine Drucknachspeisung nachkalibriert wird.
- Bei Verwendung eines Faservlieses, welches, wie bevorzugt, als Hauptbestandteil Aluminium enthält, zeigt sich ein weiterer Vorteil des beanspruchten Verfahrens. Anders nämlich als bei einem massiven Aluminiumblech, welches unter Umgebungsluft auf der Außenseite bekanntlich eine dünne Oxidhaut bildet, die sich nur aufwändig entfernen lässt und dann bei einer thixotropen Blechumformung die Gefügestruktur des Aluminiumteils signifikant verschlechtert, wird bei der Thixoumformung eines Aluminium-Faservlieses die Oxidschicht bei der Verdichtung der Aluminiumfasern aufgebrochen, so dass die Gefügestruktur im fertigen Aluminiumteil von der Oxidbildung des Ausgangsmaterials weitgehend unbeeinträchtigt bleibt.
- Die Erfindung wird nunmehr an Hand mehrerer Ausführungsbeispiele in Verbindung mit den Zeichnungen näher erläutert. Es zeigen in stark schematisierter Darstellung:
- Fig. 1
- die Herstellung eines durchgehend materialreinen Bauteils aus einem Metallfaservlies mittels einer thixotropen Druckwalzenumformung nach der Erfindung;
- Fig. 2
- eine der
Fig. 1 entsprechend Darstellung einer thixotropen Druckwalzenumformung eines Metallfaservlieses mit eingelegter Armierung; und - Fig. 3
- die Herstellung eines armierten Endlos-Blechbandes nach der Erfindung.
- Gemäß
Fig. 1 wird ein Metallfaservlies 1 aus Aluminium oder einer Aluminiumlegierung auf ein Umformbett 2 aufgelegt und dabei örtlich durch eine zusätzliche Vliesauflage 3 gedoppelt, um so eine Aluminiumteil 4 mit einer sich ändernden Wandstärke zu erzeugen. Mittels einer beheizten und in Pfeilrichtung über das Faservlies 1 gerollten Druckwalze 5 wird das Faservlies 1 im Kontaktbereich der Druckwalze 5 in den thixotropen Zustand erwärmt und so zusammengepresst, aufs dem Fasermaterial ein homogenes Aluminiumteil 4 entsteht, wobei die Lufteinschlüsse im Faservlies 1 unter der Wirkung der Druckwalze 5 in deren Laufrichtung nach vorne ausgequetscht werden und aus dem dort noch luftdurchlässigen Faservlies 1 frei entweichen können. - Um den für den Thixozustand erforderlichen Wärmeeintrag der Druckwalze 5 zu reduzieren, wird das Fasermaterial in Laufrichtung vor der Druckwalze 5 durch eine zwischen Umformbett 2 und Vliesoberseite wirksame Induktionsheizung 6 bis nahe an die Thixotemperatur vorgewärmt.
- Die Ausführungsform nach
Fig. 2 , wo die dem ersten Ausführungsbeispiel entsprechenden Komponenten durch das gleiche Bezugszeichen gekennzeichnet sind, unterscheidet sich von diesem hauptsächlich dadurch, dass in das Metallfaservlies 1 eine - in diesem Fall mehrlagige - Armierung 7 eingelegt ist, welche aus einem metallischen Fadengeflecht oder einem dicht perforierten Lochblech, aber auch aus nicht-metallischen, uni- oder multidirektional bis hin zu quasi-isotrop orientierten Verstärkungsfasern, etwa aus Carbon bestehen kann. Bei der Thixoumformung des Metallvlieses wird die Armierung 7 mit dem thixotropen Vliesmaterial dürchtränkt, so dass das Bauteil 4 eine homogene Metallstruktur mit einer in diese zumindest form- und bei einer metallischen Armierung 7 je nach Vlies- und Armierungsmaterial auch stoffschlüssig eingebundenen Armierung 7 aufweist, durch welche die Materialeigenschaften gegenüber einem reinen Einstoff-Bauteil deutlich verbessert werden. - Gemäß
Fig. 3 werden zur Herstellung eines armierten Blechbandes 8 mehrere Schichten, bestehend aus einer oberen und einer unteren, metallischen Faservliesschicht 9.1, 9.2 und einer dazwischen liegenden Armierung 10, etwa eines Carbonfasergeleges, jeweils von einer Vorratsrolle 11.1, 11.2 bzw. 12 abgezogen und zwischen zwei Vorpresswalzen 13 zusammengeführt und zu einem dichteren Materialverbund vorverdichtet. lm nächsten Schritt durchläuft der vorverdichtete, aber noch flexible Materialverbund 9, 10 eine Heizeinrichtung 14, an der er auf ein Temperaturniveau noch unterhalb des thixotropen Zustandes der Metallfasern der Faservliesschichten 9 vorgeheizt wird. Der so vorgeheizte, aber noch inhomogene Materialverbund 9, 10 wird anschließend im Walzenspalt zweier Druckwalzen 15.1, 15.2 auf den thixotropen Zustand erwärmt und gleichzeitig werden die Faservliesschichten 9 in diesem Zustand durch den Walzenandruck zu einem Endlos-Blechband 8 mit einer homogenen Metallstruktur 16 und in diese als Matrix eingebetteten Armierung 10 verpresst. - Durch die injizierte Scherrate des Druckwalzenpaares 15 wird das thixotrope Faservliesmaterial gleichförmig zum Fließen gebracht, so dass selbst feinste Strukturen der Armierungsfasern 10 von diesem umschlossen und dabei Hohlräume gefüllt werden. Hierbei bildet sich ein Formschluss und je nach Beschaffenheit des Armierungsmaterials entsteht auch ein lokaler Stoffschluss. Anschließend erfolgt noch an einem Walzenpaar 17 eine Nachkalibrierung, um eine Erstarrungsporosität zu unterbinden. Mit dieser Erfindungsvariante ist es möglich, Blechbänder 16 beliebiger Länge anzufertigen und dabei die eingelegte Armierung 10 absolut lagestabil in das metallische Vliesmaterial einzubetten. Erreicht wird dies durch die charakteristische Eigenschaft, dass das Faservlies 9 im thixotropen Zustand eine stark reduzierte Viskosität aufweist und auch die Druckbeaufschlagung im Walzenspalt des Druckwalzenpaares 15 keine unkontrollierte Positionsverschiebung der Armierung 10 verursacht.
Claims (9)
- Verfahren zum Herstellen eines metallischen Bauteils, bei dem ein metallisches Faservlies (1) auf den thixotropischen Zustand aufgeheizt und in diesem Zustand unter Druckeinwirkung zu einer kompakten Metallstruktur umgeformt wird, dadurch gekennzeichnet, dass
das Metallfaservlies (1) in den jeweiligen Grenzen des Kontaktbereich mindestens einer oberflächenseitig über dieses geführten Druckwalze (5) im thixotropen Zustand gehalten und gleichzeitig unter der Wirkung des Walzenandrucks zu einer homogenen Metallstruktur verdichtet wird. - Verfahren zur Herstellung eines fortlaufenden Blechbandes, dadurch gekennzeichnet, dass
ein Endlos-Metallfaservlies (9) im Walzenspalt zweier Druckwalzen (15.1;15.2) im thixotrop erwärmten Zustand zu einem homogen strukturierten Blechband (8) umgeformt wird. - Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet dass
in das Metallfaservlies (1;9) vor der Thixoumformung eine Armierung (7;10) eingelegt und diese im Wirkbereich der Druckwalze(n) (5;15.1;15.2) mit dem metallischen Faservliesmaterial (1;9) als Matrix durchtränkt wird. - Verfahren nach Anspruch 3, dadurch gekennzeichnet, dass
die Armierung (10) aus uni- oder multidirektional verlaufenden Verstärkung-, vorzugsweise Carbonfasern besteht. - Verfahren nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass (1;9)
das Metallfaservlies vor dem Druckwalzendurchlauf bis nahe an den thixotropen Zustand vorgewärmt wird. - Verfahren nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass
das Metallfaservlies (1;9) induktiv erwärmt wird. - Verfahren nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass
das Metallfaservlies (1;9) im Anschluss an die thixotrope Druckwalzenumformung durch eine Drucknachspeisung nachkalibriert wird. - Verfahren nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass
das Metallfaservlies (1;9) vor der Thixoumformung vorverdichtet wird. - Verfahren nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, dass
das Metallfaservlies (1;9) als Hauptbestandteil Aluminium enthält.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102011003415A DE102011003415A1 (de) | 2011-02-01 | 2011-02-01 | Verfahren zum Herstellen eines metallischen Bauteils |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2481497A1 EP2481497A1 (de) | 2012-08-01 |
| EP2481497B1 true EP2481497B1 (de) | 2013-09-04 |
Family
ID=45023709
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20110190029 Not-in-force EP2481497B1 (de) | 2011-02-01 | 2011-11-22 | Verfahren zum Herstellen eines metallischen Bauteils |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP2481497B1 (de) |
| DE (1) | DE102011003415A1 (de) |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3667496D1 (de) * | 1985-03-25 | 1990-01-18 | Osprey Metals Ltd | Verfahren zum herstellen von metallischen produkten. |
| EP1046443A1 (de) * | 1999-04-23 | 2000-10-25 | Franz Dr.-Ing. Gütlbauer | Verfahren und Vorrichtung zur Formung von Metallsträngen |
| ATE402271T1 (de) * | 2003-11-05 | 2008-08-15 | Univ Stuttgart Ct Of Competenc | Verfahren zur herstellung eines bauteils mit metallischer matrix und verstärkung durch fasern oder partikel |
| DE102007046226A1 (de) * | 2007-09-26 | 2009-04-09 | Thyssenkrupp Steel Ag | Verfahren zur Herstellung eines Leichtblechs |
| DE102009015418B4 (de) | 2009-03-27 | 2017-07-13 | Bayerische Motoren Werke Aktiengesellschaft | Verfahren zur Herstellung eines Bauteils |
-
2011
- 2011-02-01 DE DE102011003415A patent/DE102011003415A1/de not_active Withdrawn
- 2011-11-22 EP EP20110190029 patent/EP2481497B1/de not_active Not-in-force
Also Published As
| Publication number | Publication date |
|---|---|
| EP2481497A1 (de) | 2012-08-01 |
| DE102011003415A1 (de) | 2012-08-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2601028B1 (de) | Doppelbandpresse und verfahren zum herstellen eines plattenförmigen produkts mit einer doppelbandpresse | |
| DE102008041832B4 (de) | Vorrichtung und Verfahren | |
| DE102010002988B4 (de) | Verfahren und Vorrichtung zur kontinuierlichen Herstellung von Profilbauteilen aus Faserverbundwerkstoff | |
| DE102011050701A1 (de) | Verfahren zur Herstellung eines Hybridbauteils sowie Abdeckung zur Verwendung bei der Herstellung | |
| DE102009043280A1 (de) | Halbzeug und Halbzeugverbund | |
| DE2701480B2 (de) | Vorrichtungen zum Herstellen von Vorformkörpern aus Lignozellulose-Wirrfaservliesen | |
| EP3804979B1 (de) | Verfahren zum herstellen eines naturfaserverstärkten verkleidungsbauteils für ein kraftfahrzeug | |
| DE102014015414B4 (de) | Vorrichtung und Verfahren zur Herstellung eines schalenförmigen Faserverbundteils | |
| DE102008057463A1 (de) | Feder aus einem Faserverbundwerkstoff sowie Verfahren und Vorrichtung zur Herstellung derselben | |
| EP2994572A1 (de) | Walze | |
| EP1892077B1 (de) | Verfahren und Vorrichtung zur Herstellung eines Faserverbundwerkstoll-Bauteils | |
| EP2481497A1 (de) | Verfahren zum Herstellen eines metallischen Bauteils | |
| DE2713527B2 (de) | Vorrichtung zur Herstellung von Formkörpern aus mit Bindemittel gemischten partikelförmigen Werkstoffen | |
| DE102013021195A1 (de) | Verfahren zum Herstellen eines Halbzeugs für ein Faserverbundbauteil | |
| EP0985519A2 (de) | Verfahren zur Herstellung von mit Naturfasermatten verstärkten Thermoplastplatten sowie deren Verwendung zur Hestellung von Formteilen | |
| DE102011122070B4 (de) | Aufbringen von Bindermaterial auf ein Hochleistungstextil | |
| DE2131177A1 (de) | Verfahren und Einrichtung zum kontinuierlichen Herstellen von Kunststoffhohl- oder Vollprofilen | |
| EP2796744B1 (de) | Blattfeder und Verfahren zur ihrer Herstellung | |
| EP2842727A1 (de) | Faserverstärktes Verbundbauteil | |
| DE102015221261A1 (de) | Verfahren zur Herstellung eines Fasermatrixhalbzeugs | |
| DE4339742C2 (de) | Vorrichtung zum Aushärten einer Bahn einer Formmasse | |
| EP1586703A1 (de) | Oberfläche zur Behandlungseinrichtung und Verfahren zur Herstellung einer solchen Behandlungseinrichtung | |
| DE552730C (de) | Verfahren und Vorrichtung zum Herstellen von Koerpern aus Faserzement | |
| EP3656611B1 (de) | Innenausstattungsteil mit einem faserformteil und verfahren zu dessen herstellung | |
| DE102015101884B4 (de) | Verfahren zur Herstellung eines Bauteils aus einem Faser-Kunststoff-Verbund und Vorrichtung |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| 17P | Request for examination filed |
Effective date: 20130112 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B21H 8/00 20060101AFI20130313BHEP Ipc: B21J 5/00 20060101ALI20130313BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20130418 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 630198 Country of ref document: AT Kind code of ref document: T Effective date: 20130915 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502011001284 Country of ref document: DE Effective date: 20131031 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20130904 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131204 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20130904 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131205 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140104 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 |
|
| BERE | Be: lapsed |
Owner name: BAYERISCHE MOTOREN WERKE A.G. Effective date: 20131130 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502011001284 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140106 |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: BAYERISCHE MOTOREN WERKE AKTIENGESELLSCHAFT |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 |
|
| 26N | No opposition filed |
Effective date: 20140605 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502011001284 Country of ref document: DE Effective date: 20140605 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131122 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131122 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141130 Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20111122 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141130 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131204 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 630198 Country of ref document: AT Kind code of ref document: T Effective date: 20161122 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161122 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130904 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230503 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20231123 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20231130 Year of fee payment: 13 Ref country code: FR Payment date: 20231124 Year of fee payment: 13 Ref country code: DE Payment date: 20231113 Year of fee payment: 13 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502011001284 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20241122 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250603 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241122 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241122 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20241130 |